Week 9 - Project - Master Section Development
DESIGN OF B-PILLAR THROUGH CLASS-A & MASTER SECTION WITH ATTACHMENTS FEATURES
AIM :
To develop Closed Surface Model of B pillar with the reference of given class-A and Master Sections and in addition attachment features for Fixation of Parts by following OEM Design considerations by peforming draft analysis for tooling direction so that it will be easily driven out from the mold.
THEORY :
| B-PILLAR |
- B Pillar is the most complex component/structure of the vehicle body. This is because the front door closes on the B pillar while the rear door hinges onto it. The B pillar or the center pillar in vehicles is made of steel. It is welded to roof panel on top and the vehicle’s floor pan at the bottom. This pillar provides structural support to the vehicle’s roof.
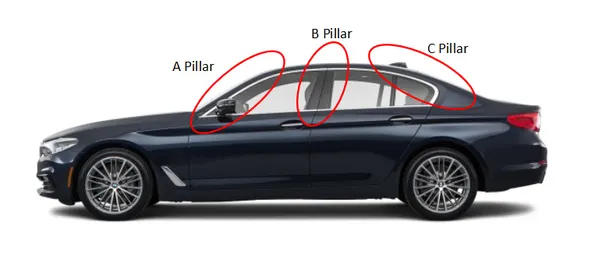 |
- Manufacturers skip the B pillar while naming other pillars. Hence, some vehicles do not have a B Pillar. The carmakers term those cars as 'Hardtops.' Instead, the vehicle specification shows the rearmost pillar as the C pillar. The manufacturers offer the Hardtops in nearly all four-door body styles. They include sedans, coupes, and wagons/MPVs. The cars without B pillars increase passenger’s visibility. However, they have limited structural support and strength. General Motors later started providing B pillars in Hardtops. Thus, it created a new vehicle body type and thereby broadened the definition of Hardtops.
 |
| MASTER SECTION |
Master sections are the guides for design requirements which decide the component packaging after technical (Styling, Concept or Class-A) surfaces. Following is the general workflow that is followed for the design and development of interior and exterior automotive trims in OEMs.
PROCEDURE :
1.Improving class-A surface (with flanges using master section) :
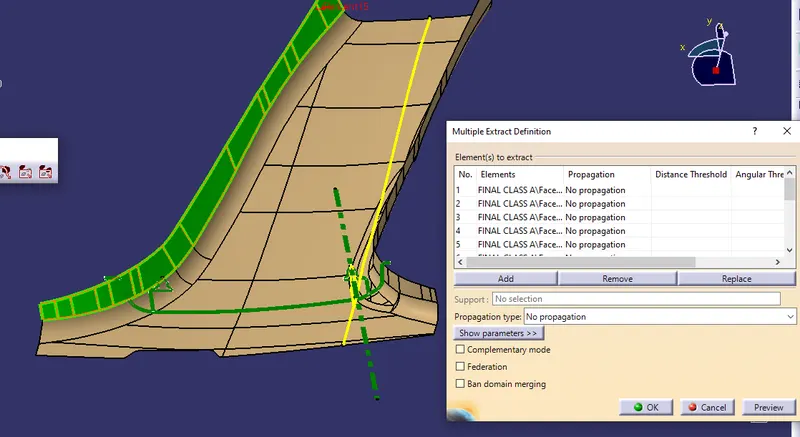
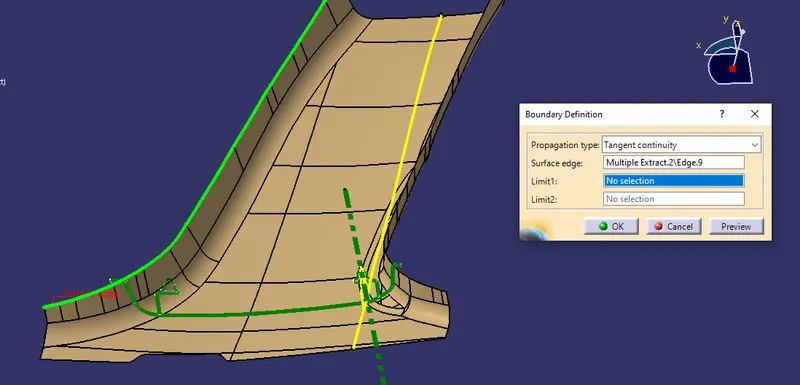
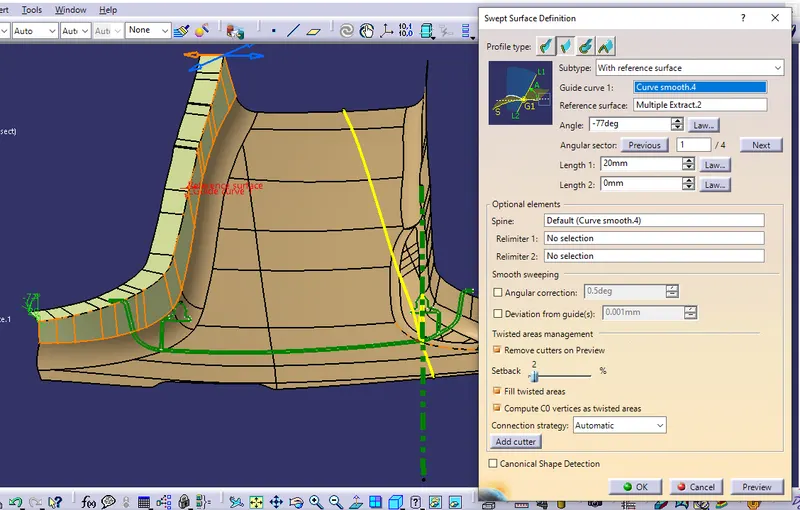
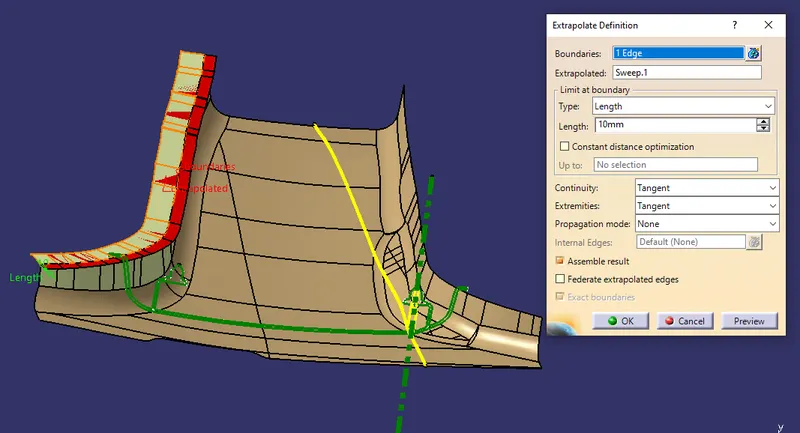
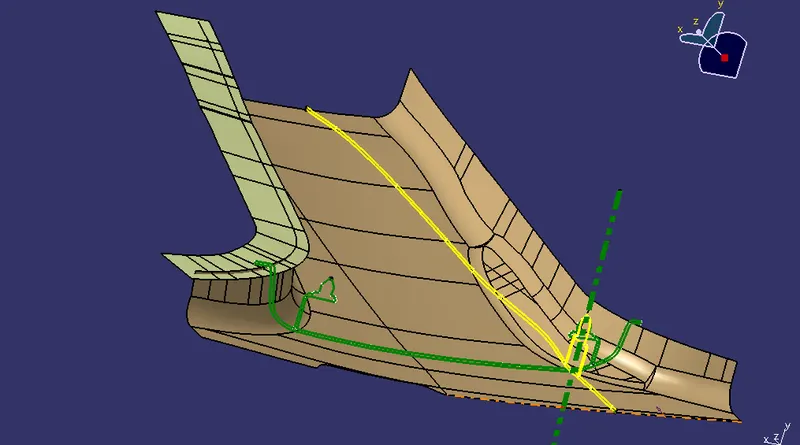
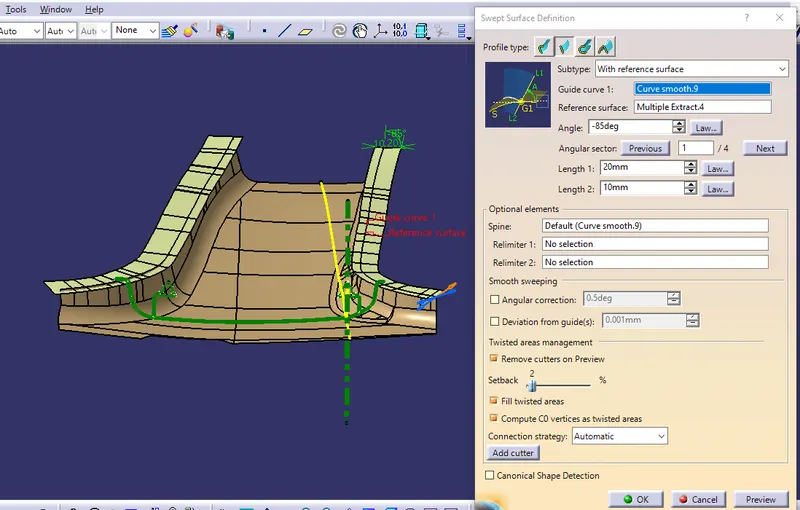
We have been given Class A surface from the styling team in this phase what we have to do is we need to develop class A with some extensions for example in this case we have to create flange and join it with A class without editing the origial class A body
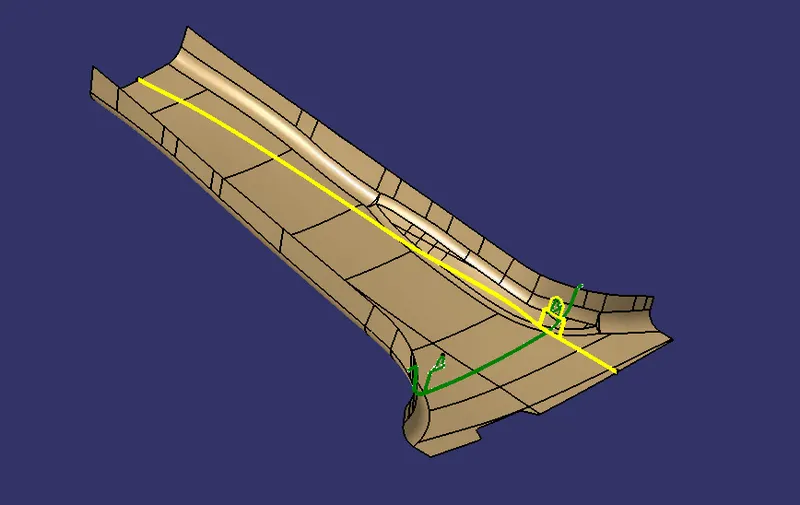
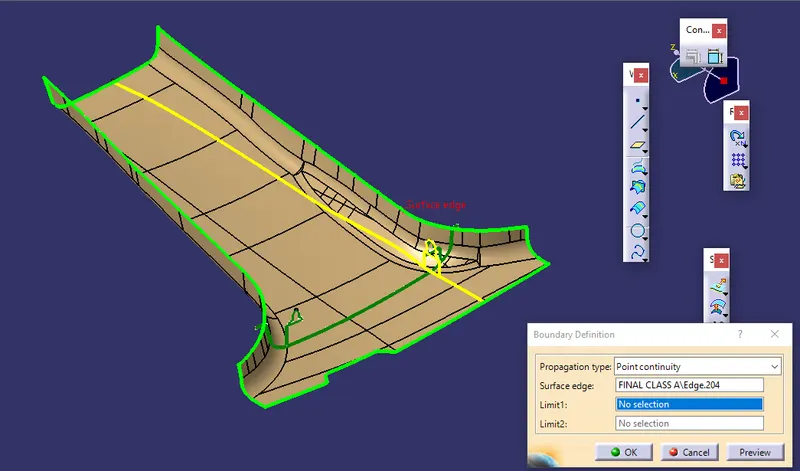
in the model we have recieved they have given master sections for reference to create the flanges and also with the help of that we will be getting the thicknees of the component where we need to it maintain while ceating class B surface and later trim them with class C to make it closed body.
2.Performing Draft analysis on class-A & Tooling axis creation
The given Class A input is analyzed to envision the part to manufacture and Tooling axis or Tooling Direction or Die line is the direction that molds pull apart in injection molding. There are two mold pieces names core and cavity. Thus tooling direction determines Mold seperation and also becomes vital in developing the plastic product which is drafted to desired nominal angle for feasible clearance and ejection of final part from the mold.
The Steps Followed in creating Tooling Axis
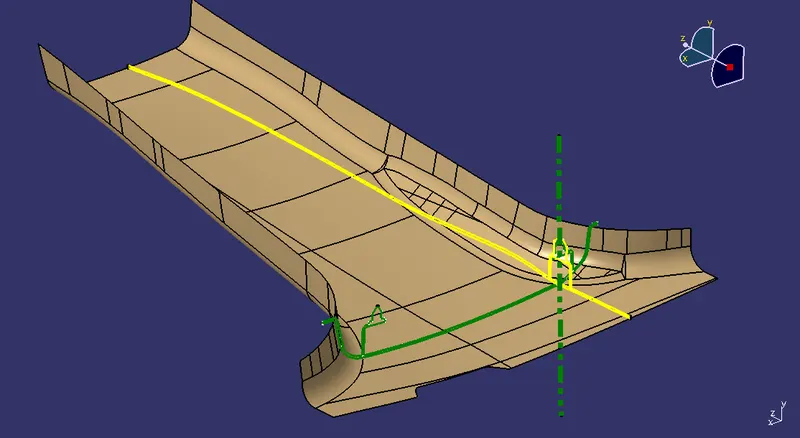
- A Reference Point is created along the Surface zero and new Axis system is created
- The X Direction and Y direction along the Class A were used to create Tooling direction
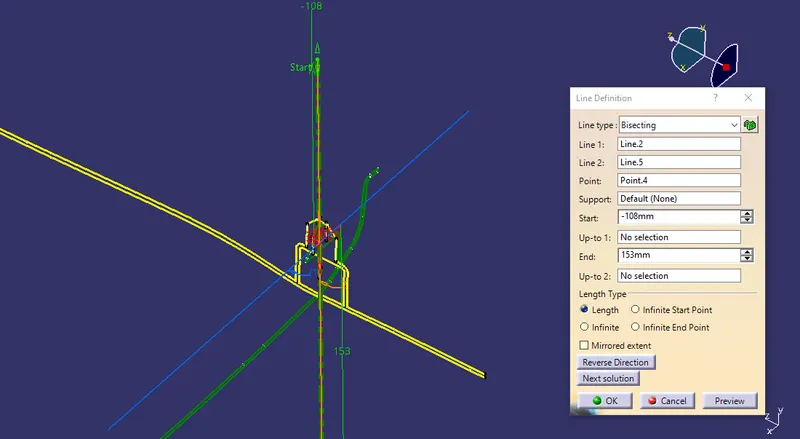
- Finally the Tooling axis is created by bisecting the two lines and it is published. Class A Surface as input using surface operation commands Class B is developed
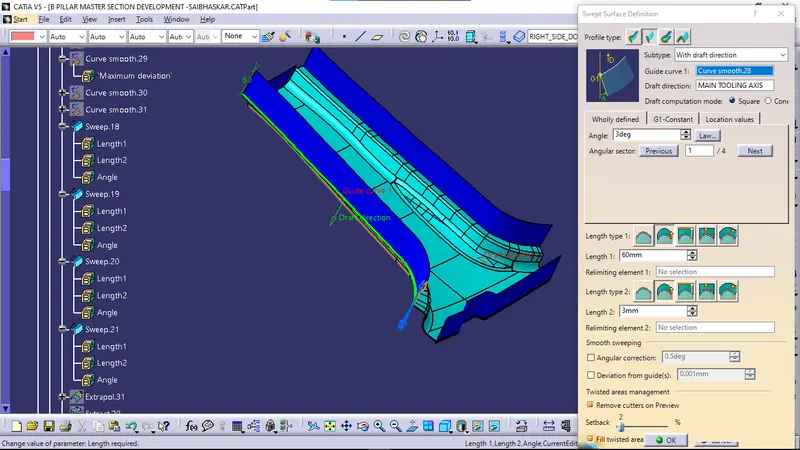
- The tooling Axis determines the direction of Class C boundary swept with draft direction.
- When viewing from tooling direction normal all the parts that are drafted should be visible so it gives an rough idea to determine product manufacturing in Injection molding
In B Pillar Model there are Two Tooling Directions one on Main tooling and other on Lifter Side that is used to eject the parts during injection modling ,Lifter Axis is used because the Attachment feature is bounded by close walls
3.Creating class-B
from the class A where we have developed it with flanges we now proceed preparing its class B where all the engineering features are mounted.here we have seen from master section that the thickness is 2mm so we should maintain thickness of 2 mm from class a to class b by creating offset
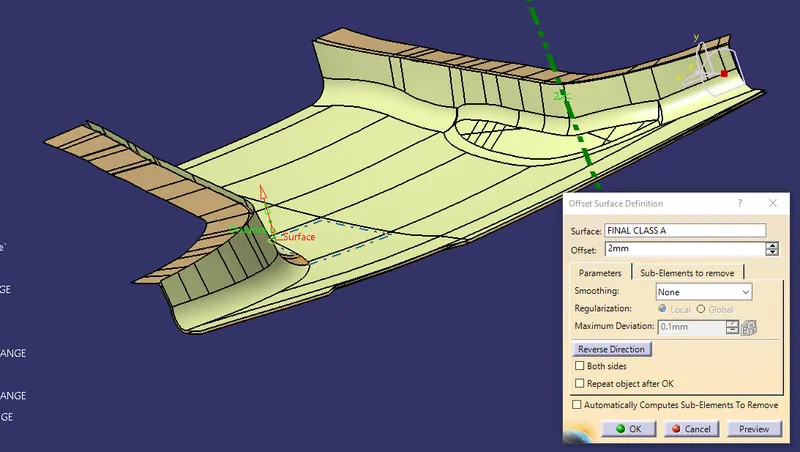
sometime the offset might not work for all the surfaces we need to fill the gaps and create missing surfaces and make sure the thickness is maintained uniformly
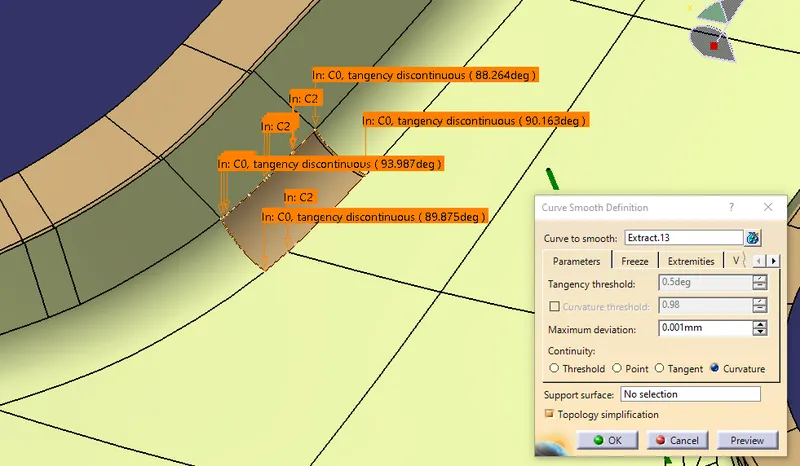
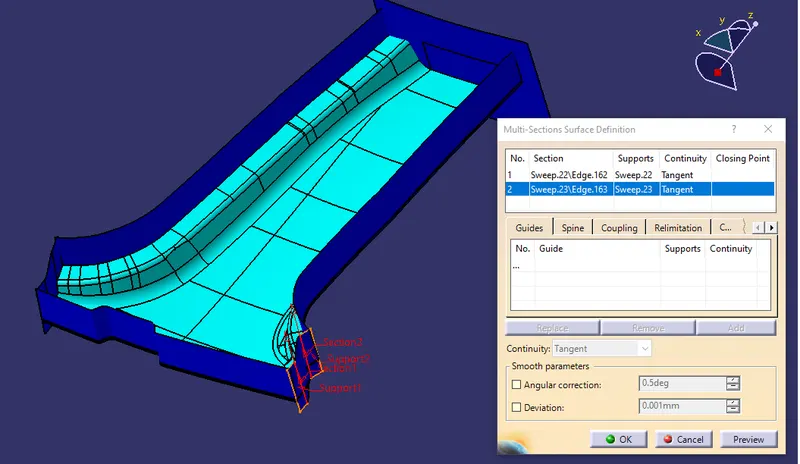
so we will make use of multisection surface ,spline ,fill,boundary,smooth,trim that are available in the surface workbench to create class B
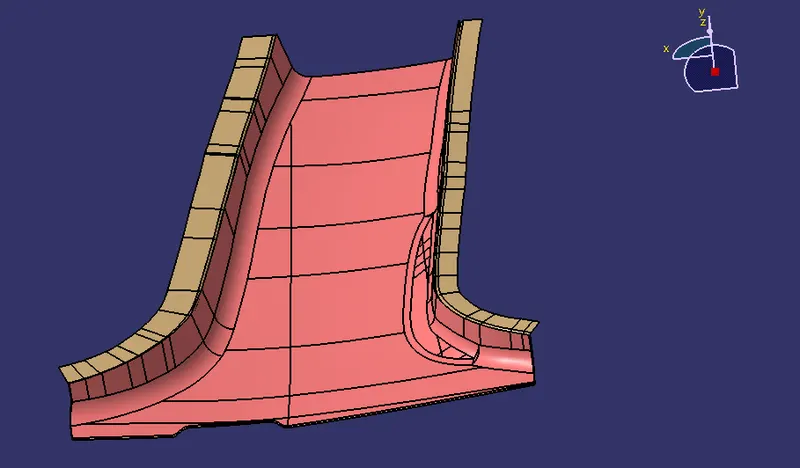
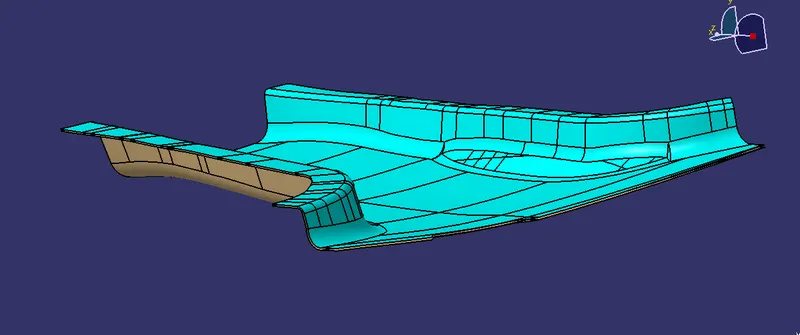
4.Creating class C (closing the body with final trim )
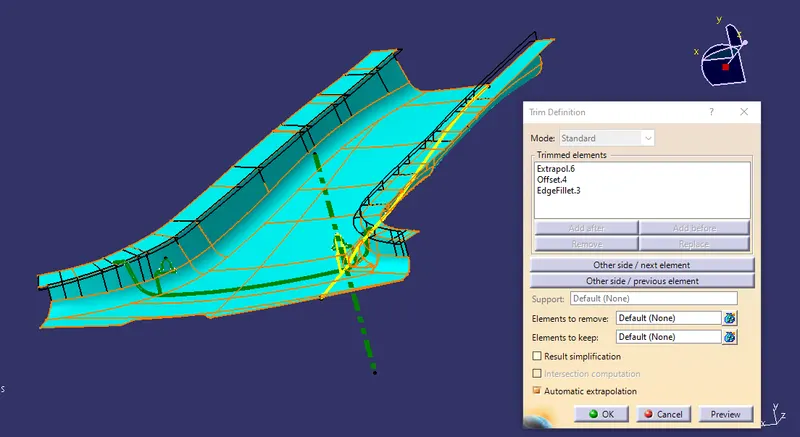
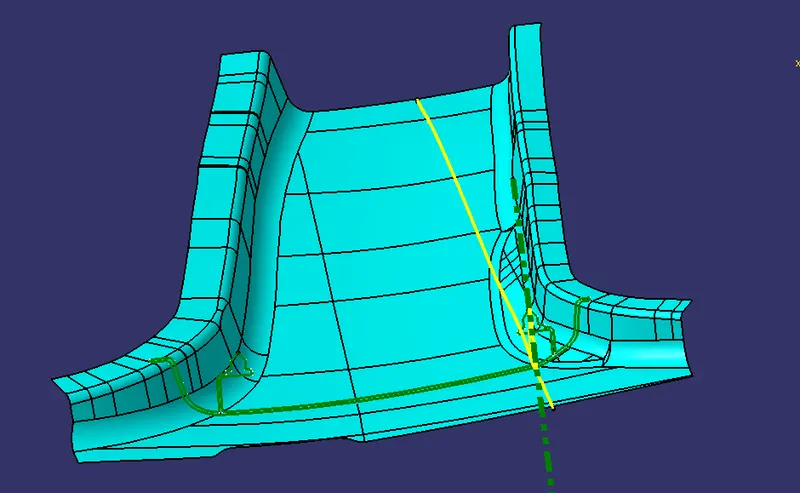
After creating class A and B now we enter to the important phase i.e., creating class C which joins class A and Class B and make it closed body
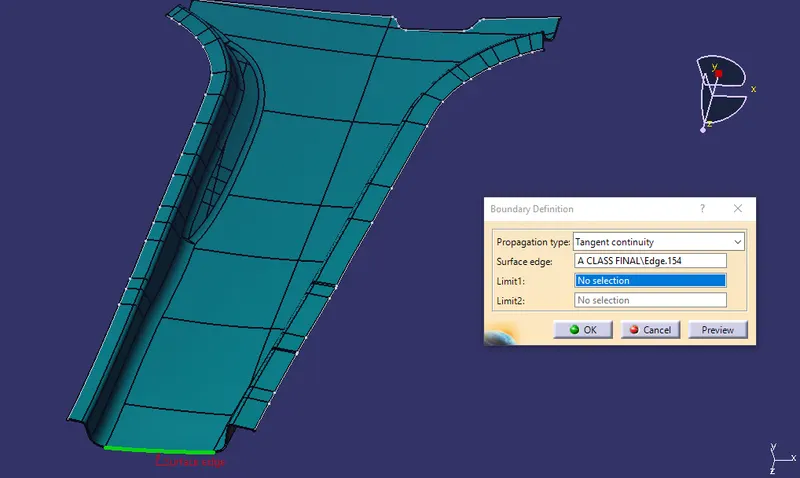
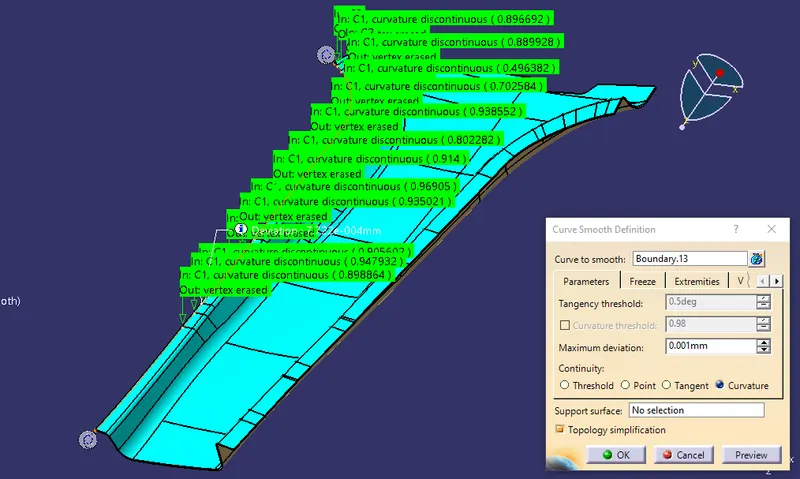
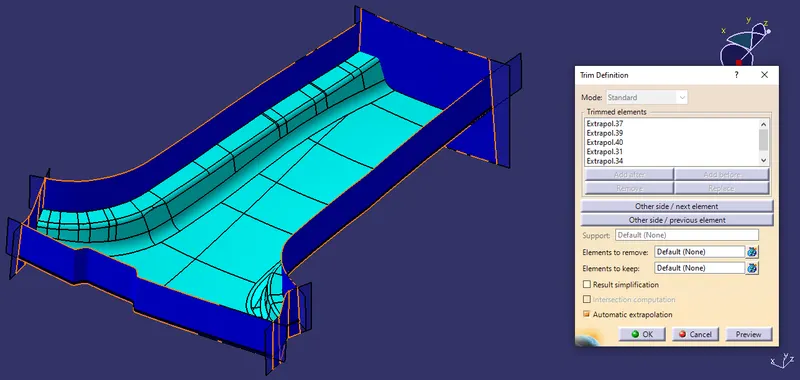
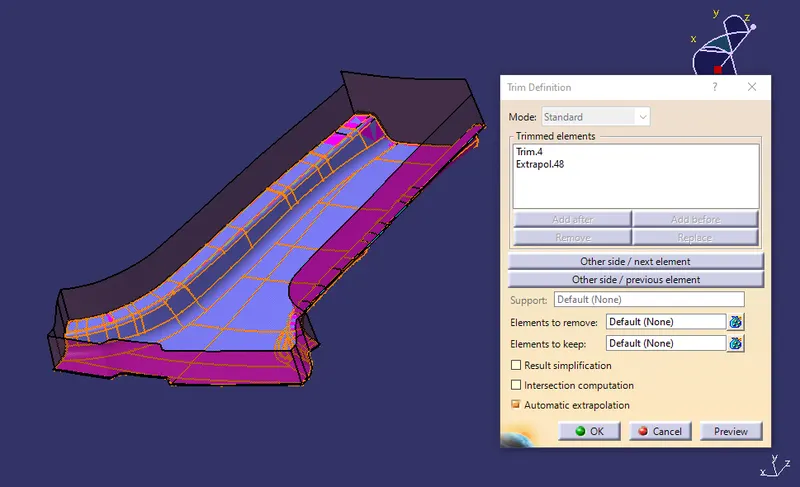
we will make use if sweep surface,blend,multisection surface to create class C by deriving the smoothened boundaries of class A nad class B. the reason we make the boundaries smooth is sometimes we might not get the result we achieved where it will crate cusp,gaps,intersections,bends etc .so we will try the best possible ways to make class C properly and later trim them as a one surface that joins class A and B.later that we will join the class C with class A and B.
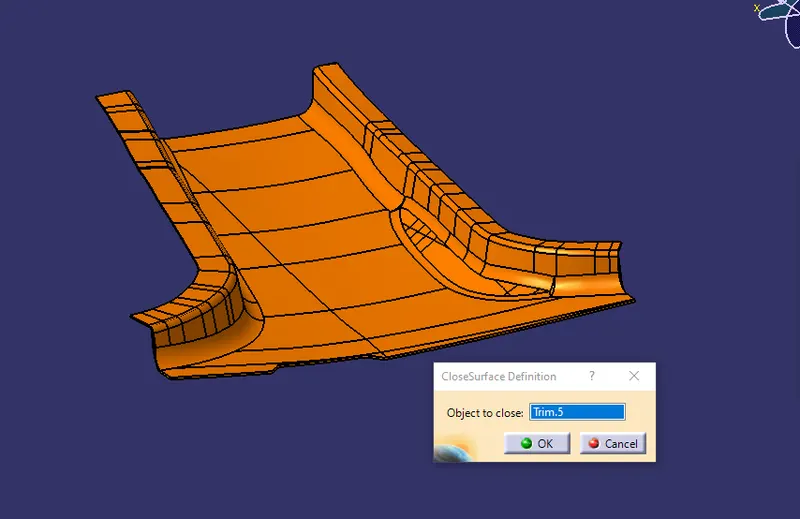
5.Creating Engineering Features :
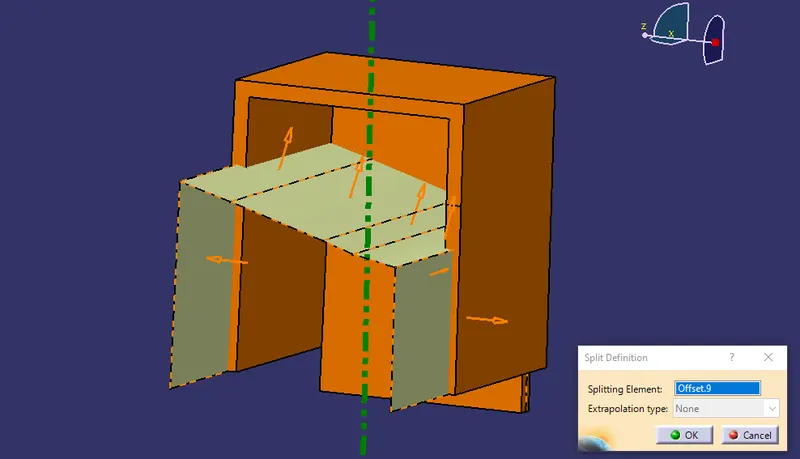
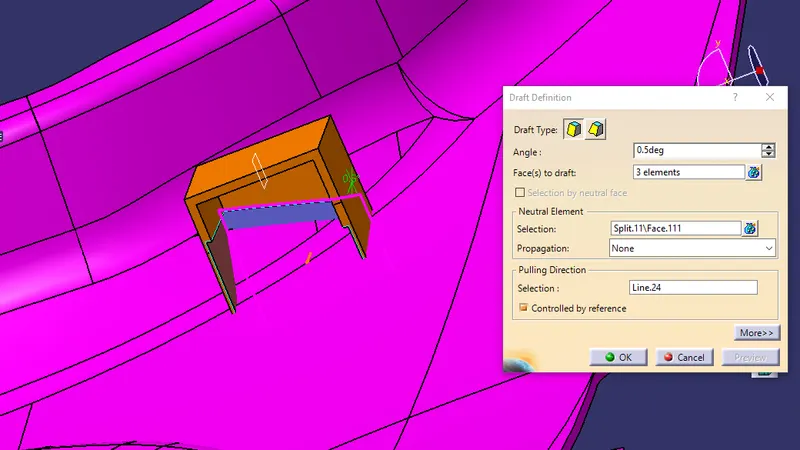
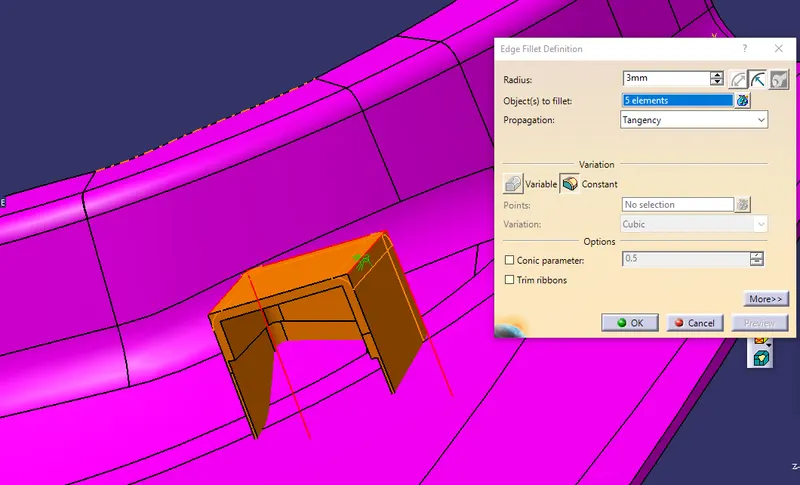
- Dog house
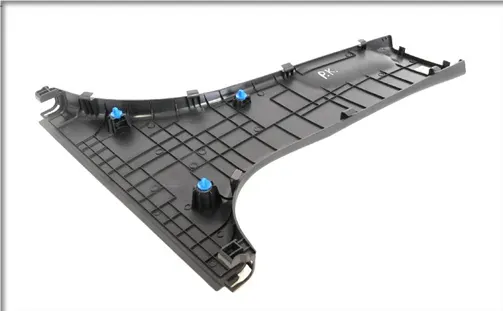
Dog house is an engineering feature used in plastic trim design. Dog houses are used as supporting feature. Sometimes other engineering features like snaps; locators etc. are mounded on them to increase their strength.Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on B-surface.
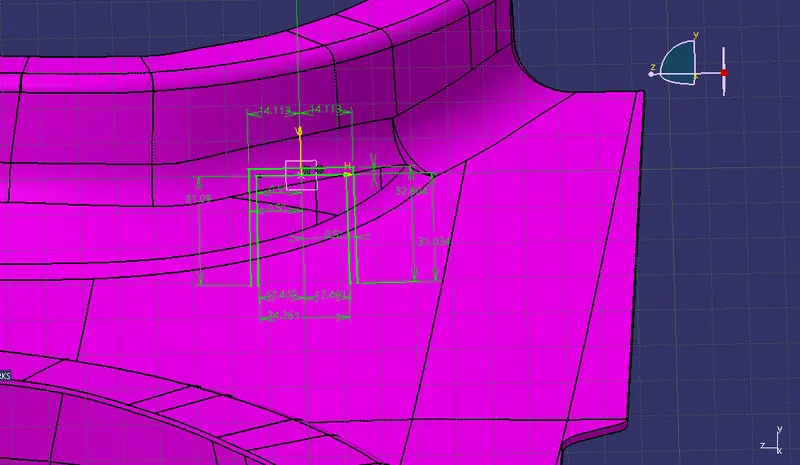
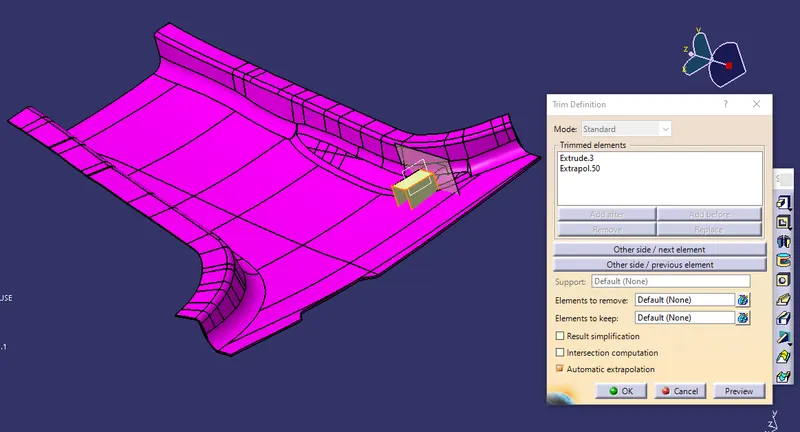
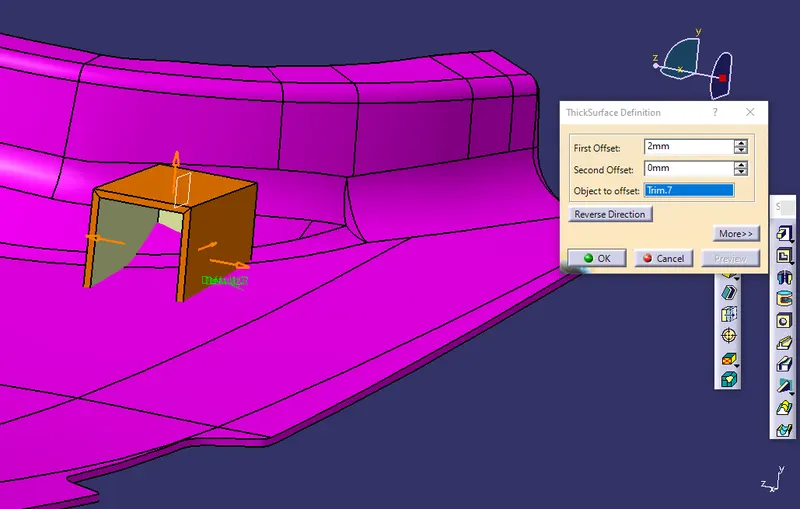
- Screw boss
Bosses are cylindrical standoffs molded into a plastic part to accept an insert or a self-tapping screw or pin for assembling or mounting parts. Bosses should be attached to a side wall or rib to enhance the structural rigidity of the part.The outer diameter (OD) of the boss should be 2 ½ times the diameter of the screw diameter for self-tapping applications.
Where extra strength is required, many designers will add internal ribs to stiffen flat walls or support external loads. Similarly, gussets are ribs which connect a boss to the floor of a part. The thickness of a rib or gusset should be no more than 60% of the overall part thickness to minimize visible sink marks on the outside of the part. For example, a part with an outer wall of 0.120” should have internal ribs at about 0.070” thickness.
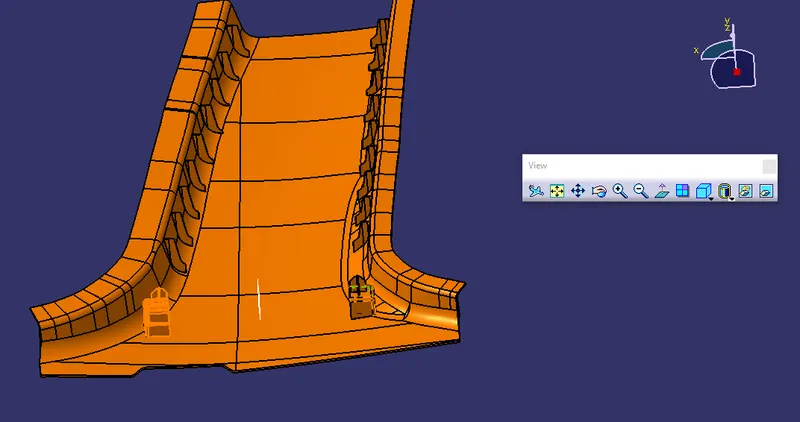
- Ribs
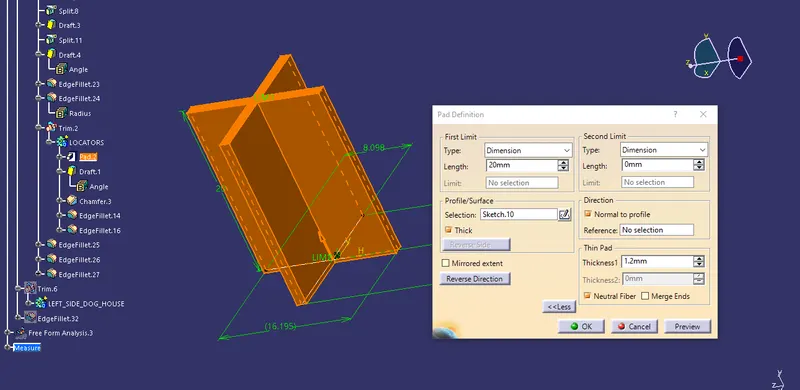
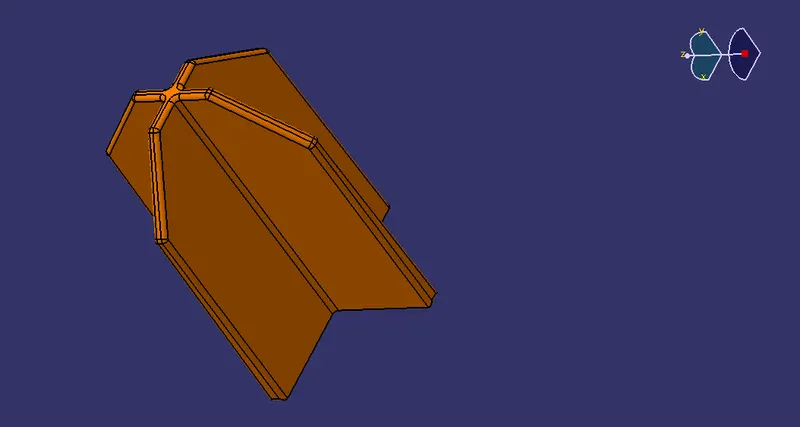
When the normal wall thickness is not strong enough to withstand the loading conditions the part is strengthened by adding ribs rather than by making whole wall thicker. Providing running ribs across the part will increase the part rigidity in all directions.These running ribs cross each other at right angle and this create a thick section at the junction which is greater than the normal wall thickness. To maintain the uniform wall thickness at the junction one way is to use a cored out boss at the junction but the most suggested is to use a normal junction with ribs that are less than 0.75 times the wall thickness. Deep ribs are structurally more efficient than thick ribs because stiffening effect of rib is proportional to cube of its depth.
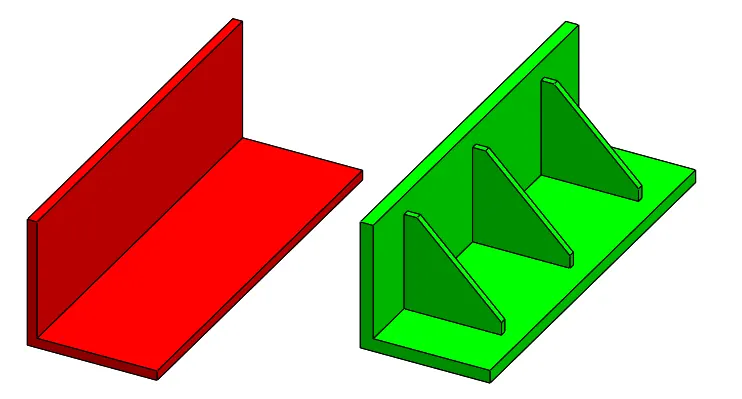
Design Considerations
• Rib thickness = 50 % to 75 % of wall thickness.
• Fillet Radius = 40 % to 60 % of rib thickness.
• Rib root thickness = 25 % of wall thickness.
• It is suggested to have deeper ribs than thicker ribs.
• Rib depth should be less than 5 times the rib thickness.
• Provide taper to ribs for their easy removal from mold.
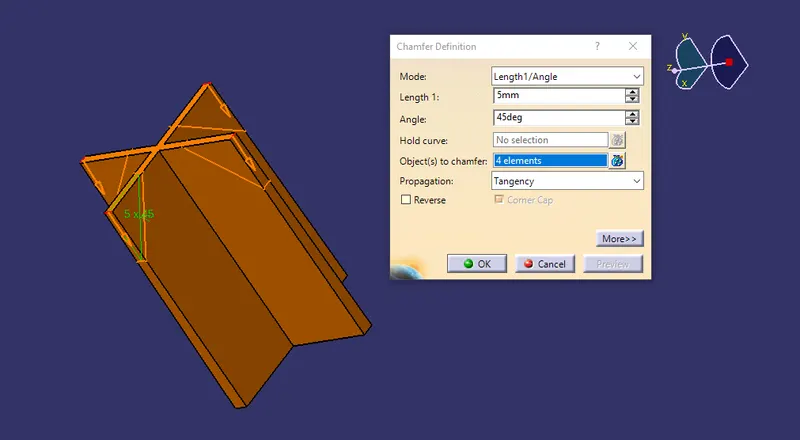
To create a rib, we first need to draw a straight line (where we want a rib) in the sketcher workbench. After creating the line, extrude it and pad it.
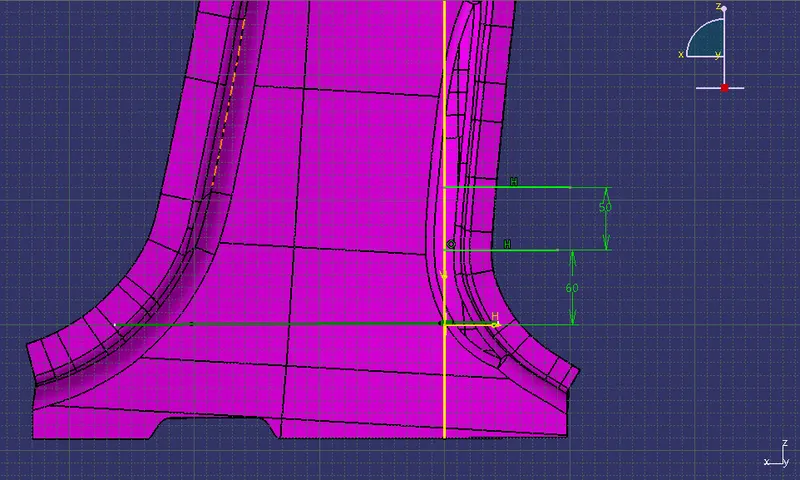
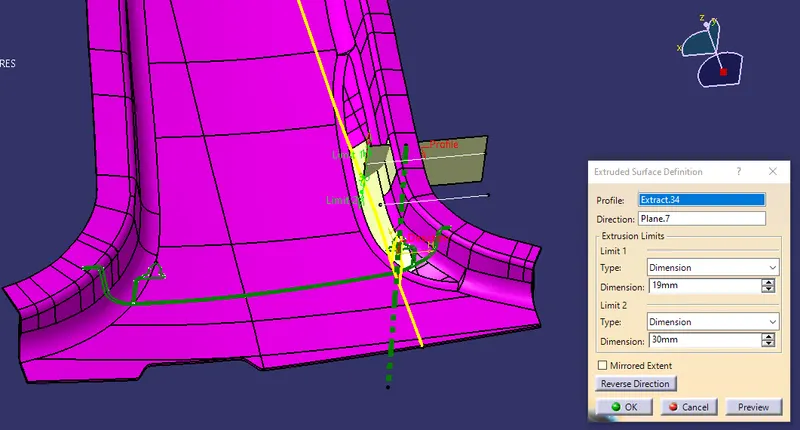
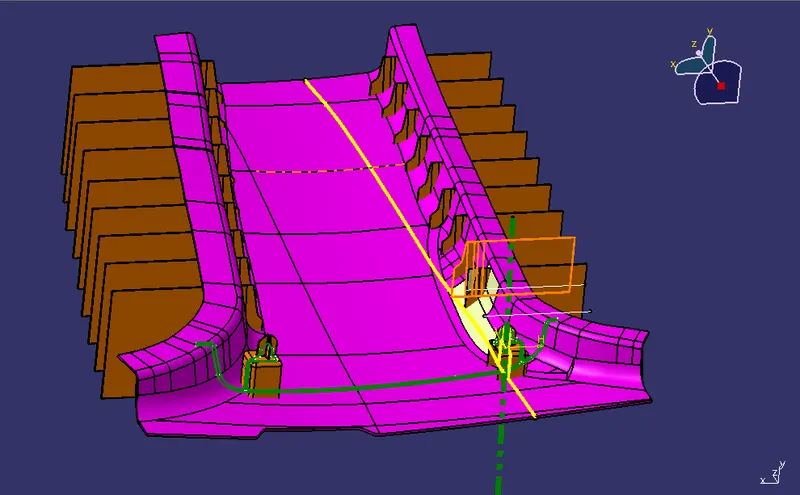
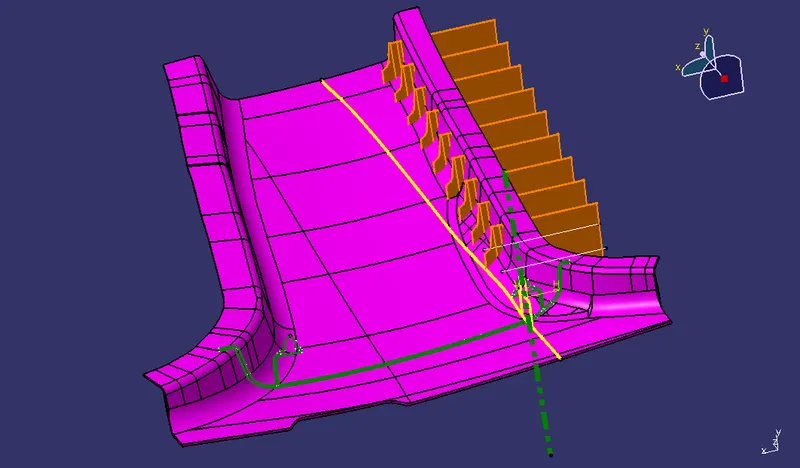
Since we need to create multiple ribs which are 50 mm apart, first go to the CLASS A / B surface and extract the boundary/edge where the flange is connecting to the main body. Now using these boundaries, create repetition points which are at a distance of 50mm from each other.
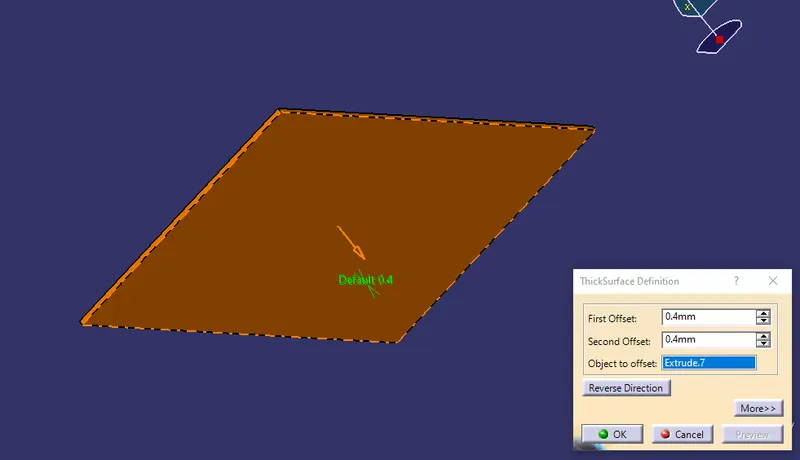
Now copy the rib (solid body) which we created and paste it in the main tree structure. Using the translate option the copied rib can be moved from one point to another. Repeat the above step for creating all the ribs and position it on the points that we have created using the repetition points option.
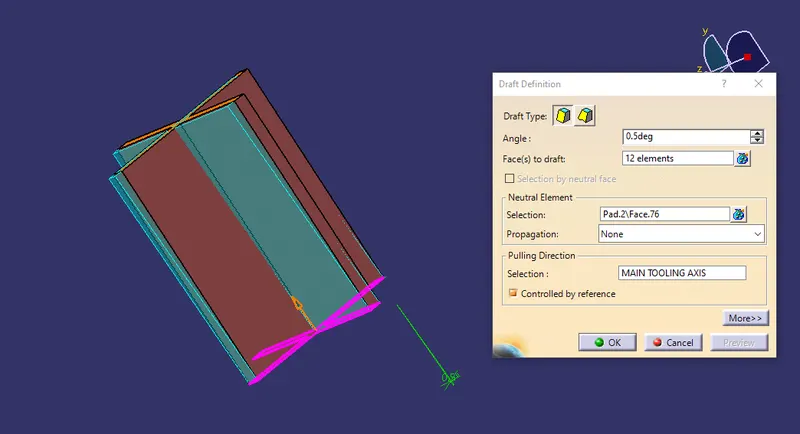
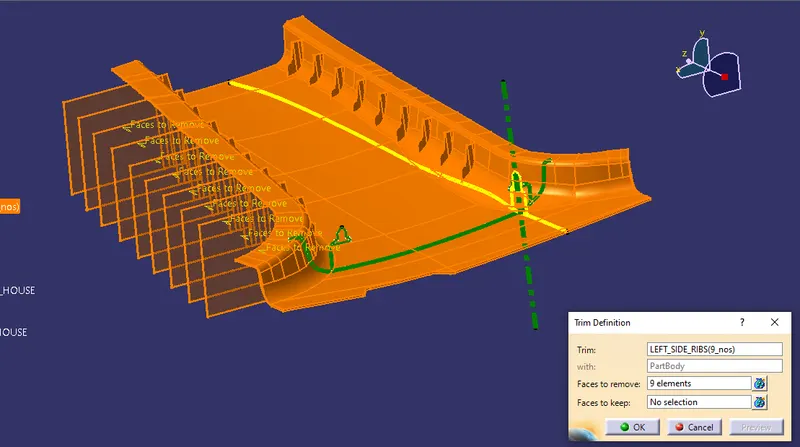
Offset the CLASS B surface to 10 mm and trim the ribs with it removing the excess portion of the ribs and give a draft of 0.3 to the ribs.
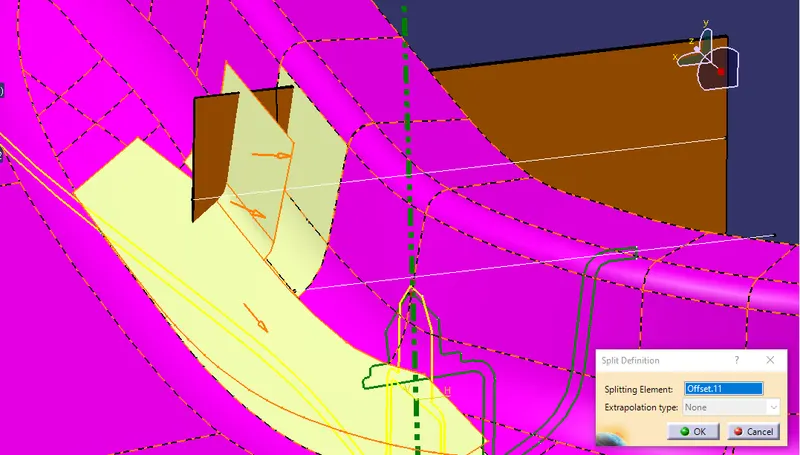
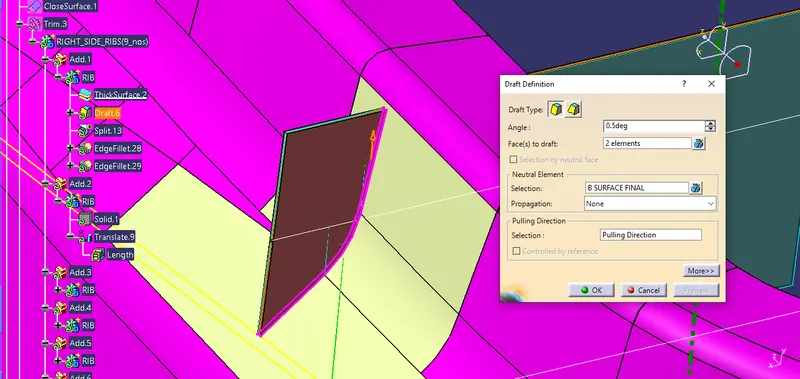
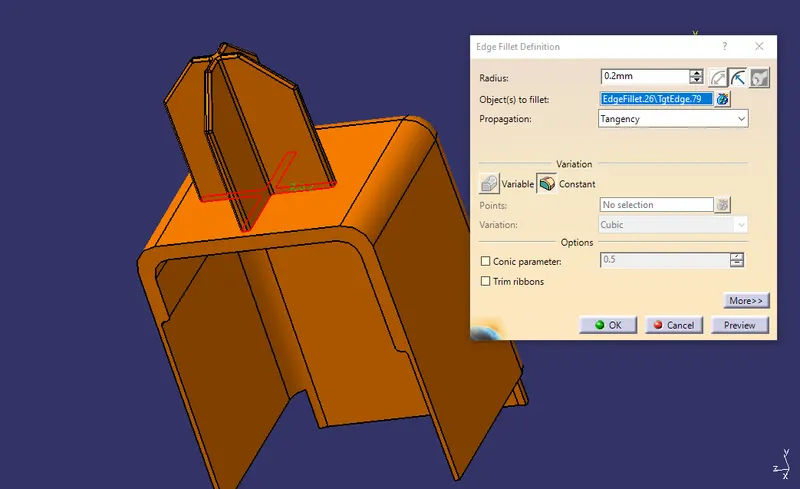
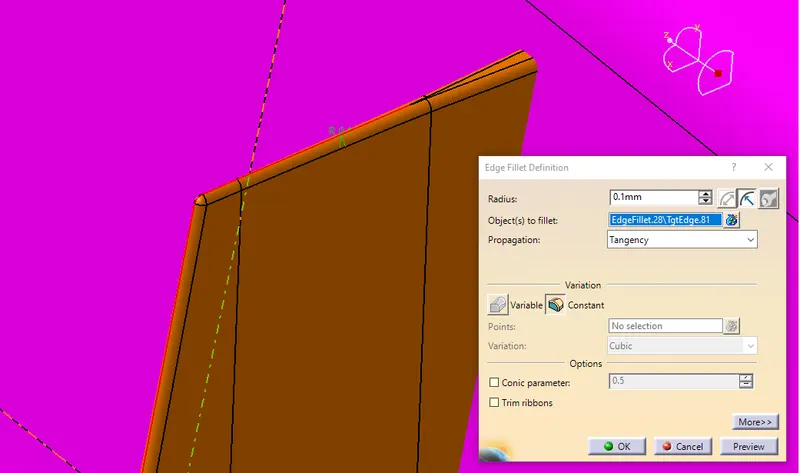
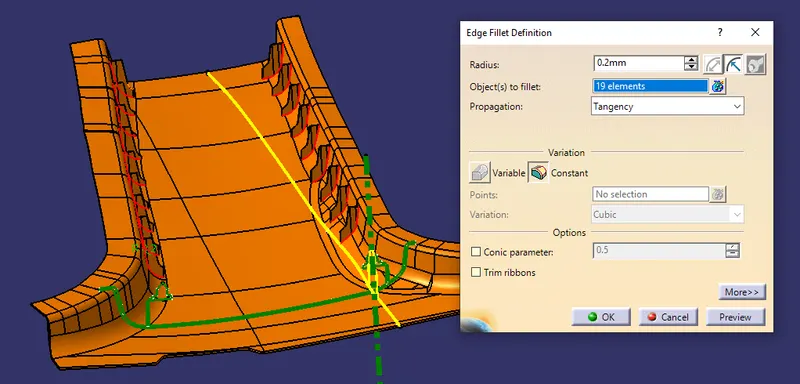
Once all the engineering features are created, add it /trim it to/with the main body i.e, B Pillar and give appropriate fillet value to all parts of the body.
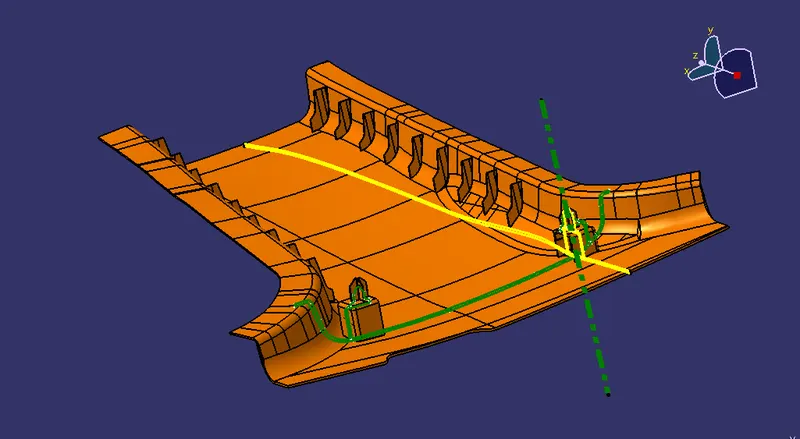
6.Draft analysis on final model :
Here we are looking at the class A surface along with master section recieved from the styling team .from here we have to develop the class B and class C. here in the class A we have missed some parts of the surface where we are going to repair them i.e., by using the tools available in the surface workbench like multisection,fill,spline and join we are join to create a complete surface without any gaps or voids ,then later we make sure there that the body have no missing surface by just checking the boundary option.
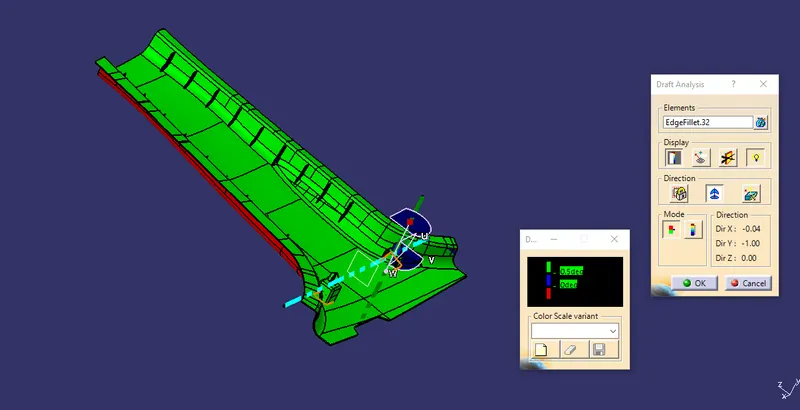
fig : Draft analysis with main tooling axis
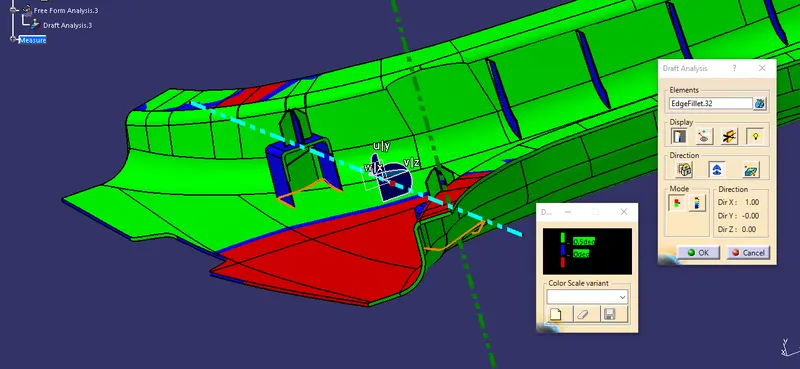
fig : Draft analysis with lifter tooling axis
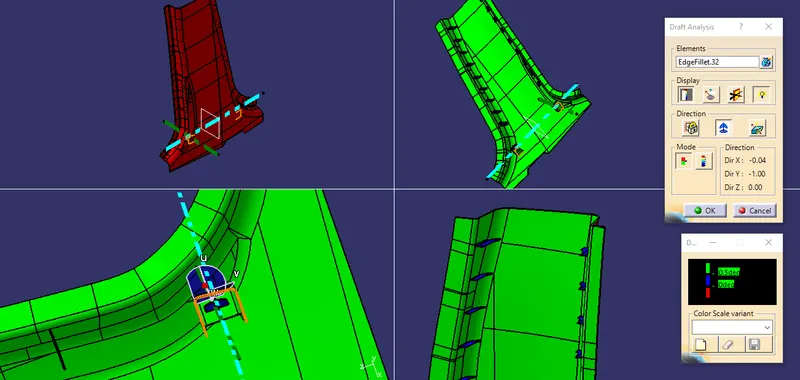
note :
i have made the following Points below to ensure:
In Tree Structure
using surface command.closed body command to create the solidsRenamed geometrical set properly.
Output Required in a report :
Picture of the sketches with Sketch solving status’s geometry tabPicture of the Detailed tree structure.Picture of the 3D CADCreate closed bodyCreate tooling axis and follow design rules.Follow the Master section to create flangeFollow the master section for thickness and to create the Closed volume.Follow master section to create Attachment features
RESULT :
- Finally we have made class B and class C from class A and make it as a closed surface model along with flanges development and engineering attachment features like dog house,4way locator,ribs etc for increasing strength to the product and for fixation purposes.
- Tooling axis have been created with the help of master section and draft analysis have been made to detect if the part we have drafted will be easily removed from the mold.