Week 9 - Attachment Feature Creation - Challenge 2
SCREW BOSS AND DOGHOUSE DESIGN:
SCREW BOSS:
Screw boss is the feature in which the bolt is bolted while assembling to the parent part. In other words, screw boss is the female part of the bolt where the bolt gets fastened.
DOGHOUSE:
Doghouse is a support feature for the other engineering features like locating pins, Screw bosses etc on the B side surface of the plastic component. Whenever these engineering features need to reach the distances of more that five times that of base thickness the feature will become weaker and tend to fail due to the bending moment, to avoid this failure they were mounted over the dog houses where about half of distance will be covered by the doghouse.
DESIGN CONSIDERATIONS:
While designing any part we should consider the manufacturing process and we should try to avoid the defects which will arise in manufacturing by proper design of the product. The plastic parts were usually manufactured in injection moulding process. Some of the common injection moulding defects listed below.
- Flow Lines
- Sink Marks
- Vacuum voids
- Surface delamination
- Weld Lines
- Short Shots
- Burn marks
- Warping
- Jetting
- Flash
In the defects listed above the ribs, Screw boss and doghouse were commonly prone to Sink marks and Short Shots. To avoid these defects in manufacturing process some of the design rules were listed below
SCREW BOSS:
Wall thickness:
Usually, thickness of the wall should be maximum 40% of the wall thickness. This is decided to avoid the sink mark on the visible surface. If the thickness of the rib at the base is high, it will increase the thickness at the junction therefore this will retain more heat than other surface. Due to this when it cools slowly it will try to shrink the material which is outside this region. Since the area at the fillet have high strength, it will shrink the flat surface causing the sink marks.
Wall Thickness at Top:
Thickness of the wall at the top must be maintained at least 0.75mm so that molten metal can flow easily. If the thickness is reduced further, it becomes difficult for the molten plastic to reach those corners of the ribs as they are almost perpendicular to the flow direction. They will leave unfilled mold region which leads to the defect called short shots.
Draft Angle:
Draft on the surfaces of the ribs is provided to ease of ejection of the part from the mold. Usually, 3-degree draft is provided on the part but in the engineering features like ribs, doghouse, Screw boss etc, were provided with minimum draft angle of 0.5 degrees.
Wall Height:
Wall height to inner diameter ratio can be maximum of 3 and preferably this ratio is maintained at 2.
Wall base fillet radius:
Maximum fillet radius allowed at base of the screw boss is 0.25mm.
Inner core depth:
Inner core depth should be maintained at the same level as base. If it is too long it will reduce the wall thickness of the base and if the core is too short, then it will have bulk material which causes sink mark while cooling.
DOGHOUSE:
Base wall thickness:
Wall thickness if doghouse where it is attached to the part must have the thickness maximum of 40% of the wall thickness. The distance B should be maintained between 3 to 6mm.
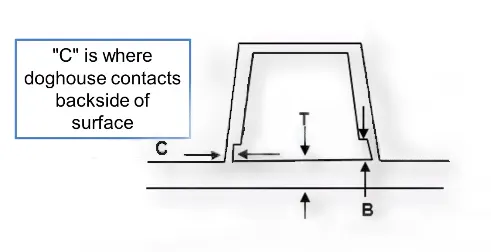
Doghouse dimensions:
Doghouse height must be at least 6mm and its width must be minimum of 12 mm. Width to height ratio can be maximum of 3 and it is preferred to be maintained at 2.
Draft Angle:
Draft angle for the outside walls of the doghouse should be maintained at 1.5 degrees and the inner wall draft should be minimum of 0.5 degrees.
PART DIMENSIONS:
Wall Thickness:
Wall thickness of the screw boss must be less that 60% of the base thickness. Here thickness should be less that 1.5mm in this model since we have 1.27mm wall thickness it conforms to the thickness rule. The inner diameter of the screw boss is provided 6.8mm considering the M8 bolt and the thickness provided 1.5mm due to the draft it has changed to 1.27mm.
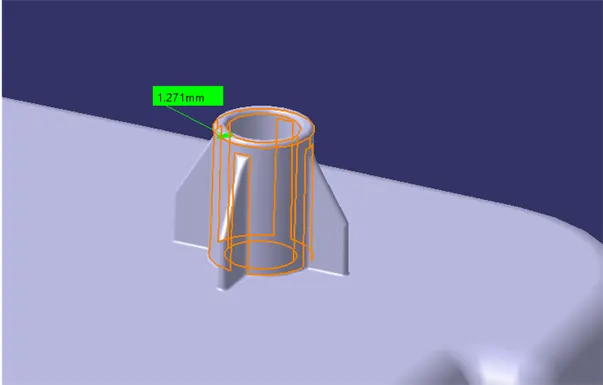
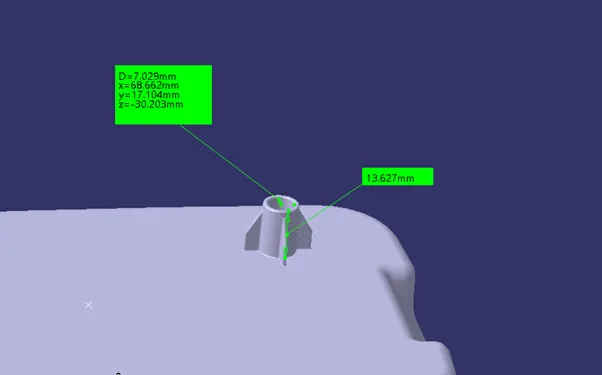
Height to Diameter ratio:
Height to diameter ratio can be maximum of 3 and preferably it is maintained at 2mm Here the screw boss is designed for M8 bolt therefore the inner diameter is maintained at 6.8mm. Then height is kept at 13.6mm with height to diameter ratio as 2. But due to the draft provided on the inner diameter the diameter measured to around 7mm and the ratio changes to 1.91 which is less than 3. Thus, conforms to height to diameter ratio.
The ribs provided as a support for the screw boss, and they were designed based on the design rules for ribs.
Base wall thickness:
The wall thickness is less that 40% of the base and the slot height is 4.5mm and fall between 3mm to 6mm rule.
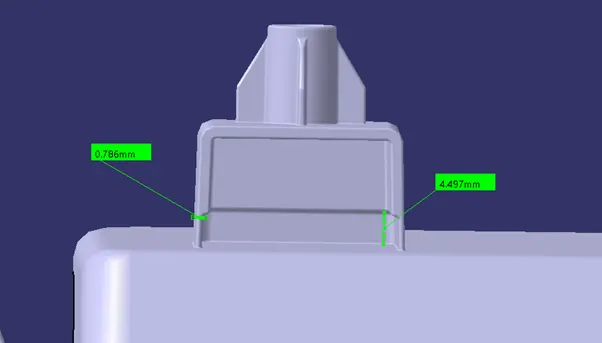
Doghouse height to width ratio:
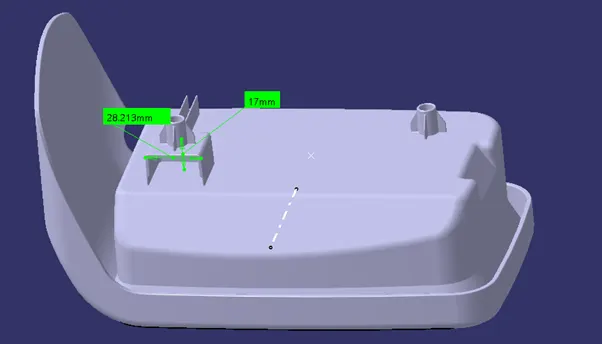
The height must be minimum of 6mm, and the width of the doghouse should be minimum of 12mm. Since we have height of 17mm and width 28.21 mm it passes the above said criteria. The ratio of width to height should be less that 3. In this case we have the width to height ratio 1.66.
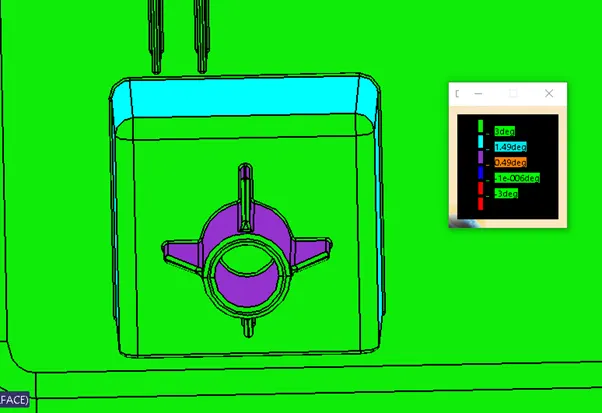
Draft for the outer walls of doghouse:
The outer wall of the doghouse clearly has the draft angle 1.5 degrees shown by colour scale.
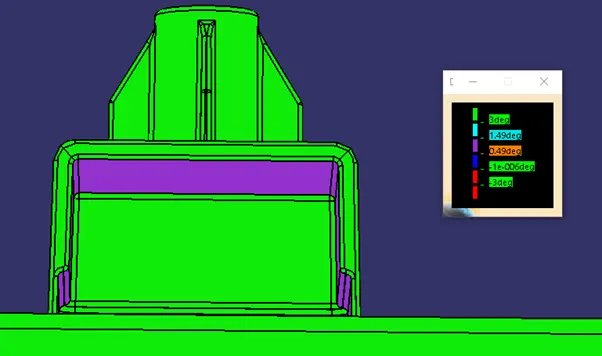
Draft of inner walls of the doghouse:
The inner walls have 0.5 degrees of draft for the side core.
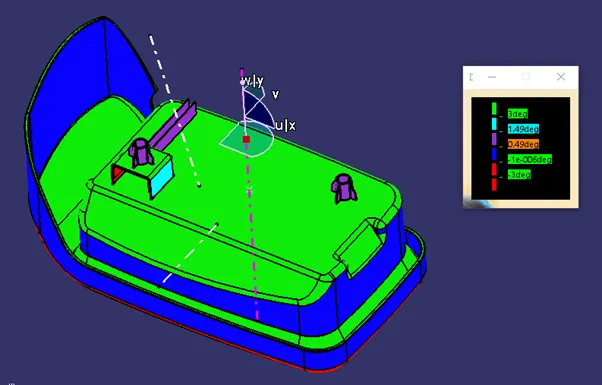
Draft of the screw boss and ribs:
The surface with 0.5 degrees of draft were highlighted in violet colour. Thus, the image clearly shows the ribs, and the screw boss is having the draft of 0.5 degrees.
ORIENTATIONS:
Front View:
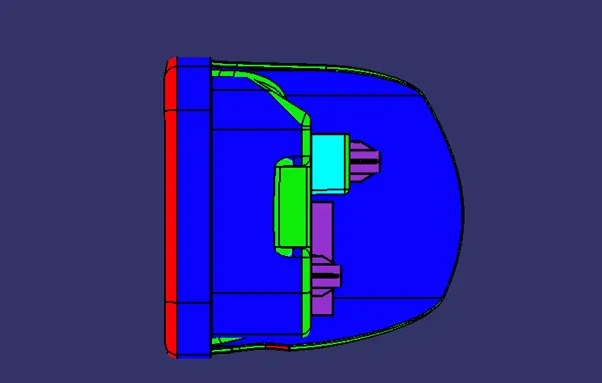
Side View:
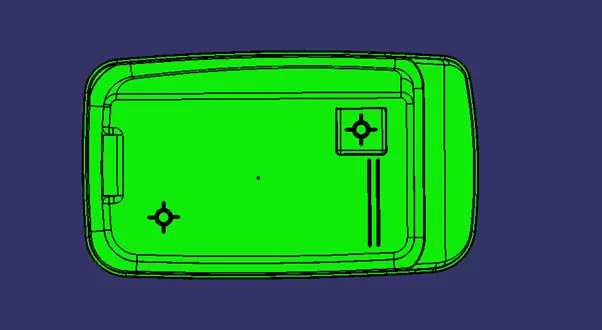
Top View:
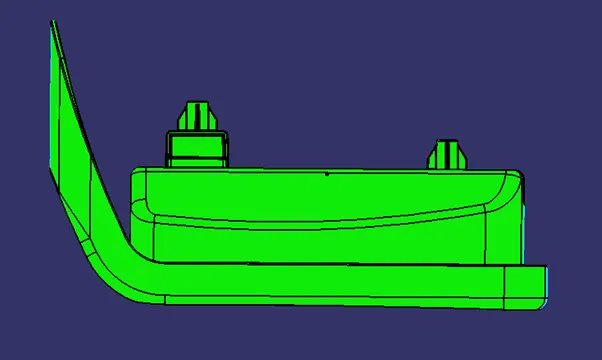
Isometric View:
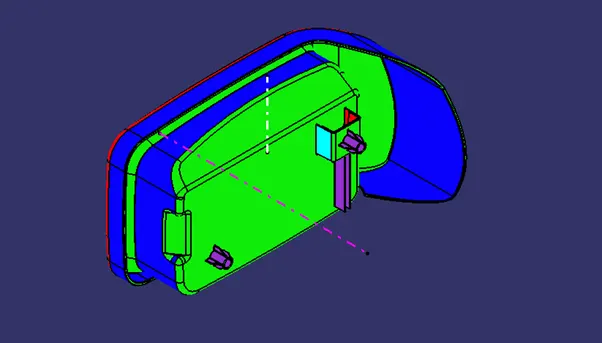
CONCLUSION:
Thus, the screw boss and the doghouse are designed based on the design rules formulated to avoid manufacturing defects in injection molding process.