Design of backdoor
BACK DOOR DESIGN
Aim
Use the provided styling surface to come up with a back door design, use appropriate design methodologies, and provide the necessary reinforcements and embosses.
Objective
1 – Learn about design consideration for back door design.
A - Visibility Criteria
B - Force Dissipation
C - Latch and Stricker Positions
D - Hinge Position
E - Gas Stay Position
F - Hemming and Relief Areas
G - Crash Analysis
H - Bend Test, Dent Test, Torsion Test & Endurance Test
I - Rear Crash Regulation
2 – Learn manufacturing process of back door.
A – Deep Drawing
B - Embossing
C - Hemming
D - Blanking and Punching
E – Gluing (Mastic and Hemming Glue)
3 – Learn about components of Back door and its significance.
A - Backdoor Outer Panel (Upper)
B - Backdoor Outer Panel (Lower)
C - Backdoor Inner Panel
D - Hinge Reinforcements (LH & RH)
E - Gas-Stay Reinforcements (LH & RH)
F - Latch and Striker Reinforcement
G - Wiper motor Reinforcement
Back Door
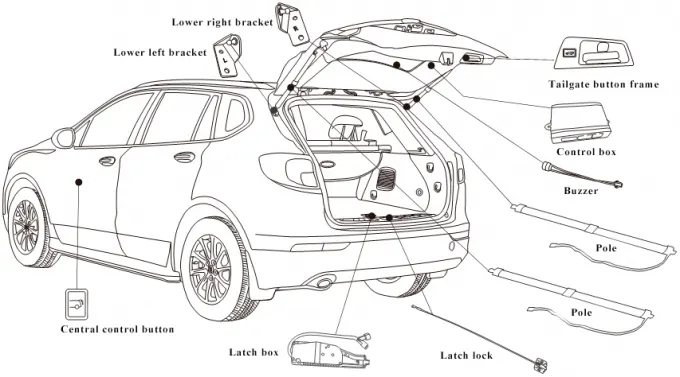
About - Back door is also called as tailgate. Back door in a car gives the access to luggage area and few cars have passenger compartment too.
Types of Back door
1 - Top mounted
2 - Side mounted
3 - Bottom mounted
Top Mounted
1 – Mounted with roof of the car & with C Pillar by gas stay/Power lifter.
2 - Advantage of this type of back door is it provides greater rear visibility compared to others.
Side Mounted
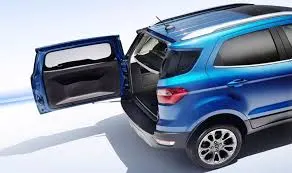
1 - Side mounted doors are mounted on the side of the car. (SUV, Vans & Trucks)
2 - Accidental head impacts can be avoided with this type. It is easier to load and unload items using this door.
Bottom Mounted
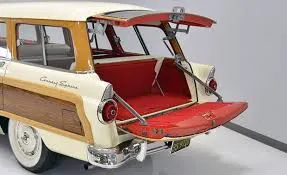
1 - This is the most comfortable type of back door; it can be also used as supporting table or holding long items.
2 – Used in pickup trucks and some luxury SUVs.
Based on Working mechanism
1 - Powered lift type
2 - Gas stay type
Powered lift type
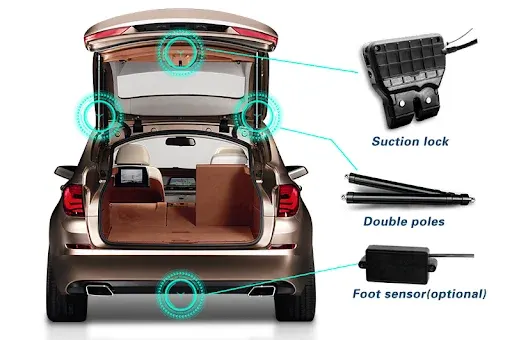
1 - Powered lift type is also known as electric motor actuated type. It is mostly used in luxury cars.
2 - This consists of power latch, anti-pinch switch, PTF assembly. Open the door automatically.
Gas stay type
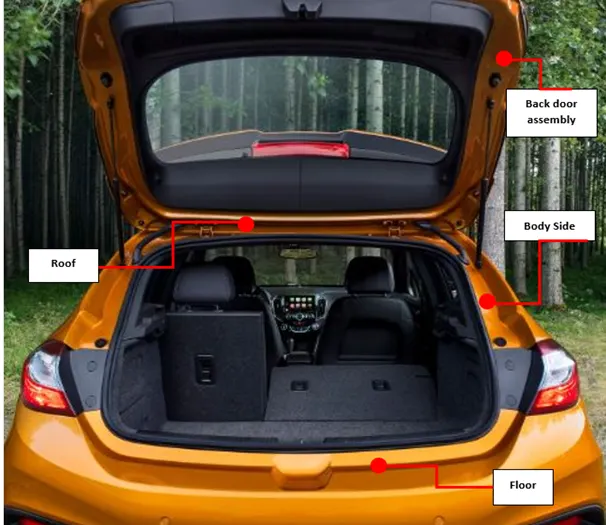
1 - Gas stay type is the most common type used in cars for operating the back door. Components of back door are gas stay, hinge, wiper mechanism.
Manufacturing Process
Various manufacturing process, like bending, stamping, punching, deep drawing, hemming, embossing, spot welding and even more operations use for back door design, But the main objective is to reduce the time, cost & increase productivity.
Bending
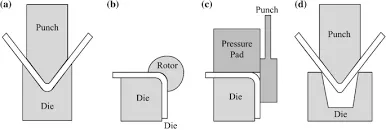
In bending the sheet metal is bent to a defined curvature. Here simple curve surfaces are produced and this becomes the base surface of the component. A Die and Press arrangement applies pressure on the sheet metal which changes the curvature of the blank permanently. And applying of pressure must be careful that the metal should not spring back to its original shape.
Deep Drawing
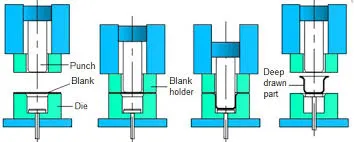
Next after the bending process drawing operation is done here Complex curvature can be produced. the die and the mould create the desired shape which we predefined for the blank the pressure is applied hydraulically or mechanically that forces the punch to the die and forms the shape in the sheet metal. Negative draft angle is avoided because it cannot be manufactured. One of the drawing processes is Deep drawing, deep drawing is a forming operation this is a combination of tensile and compression.
Stamping
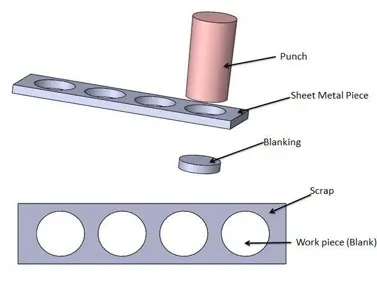
Stamping is done with the help of Stamping press machines share a series of dies or a single die with various cuts or formed on the metal.
Embossing
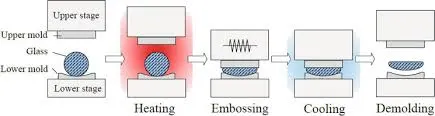
Embossing is a metal forming process for producing raised designs in sheet materials with the help of dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female dies producing a pattern or design on the metal sheet. Depending on the dies used, different patterns can be produced on the metal sheet.
Lancing
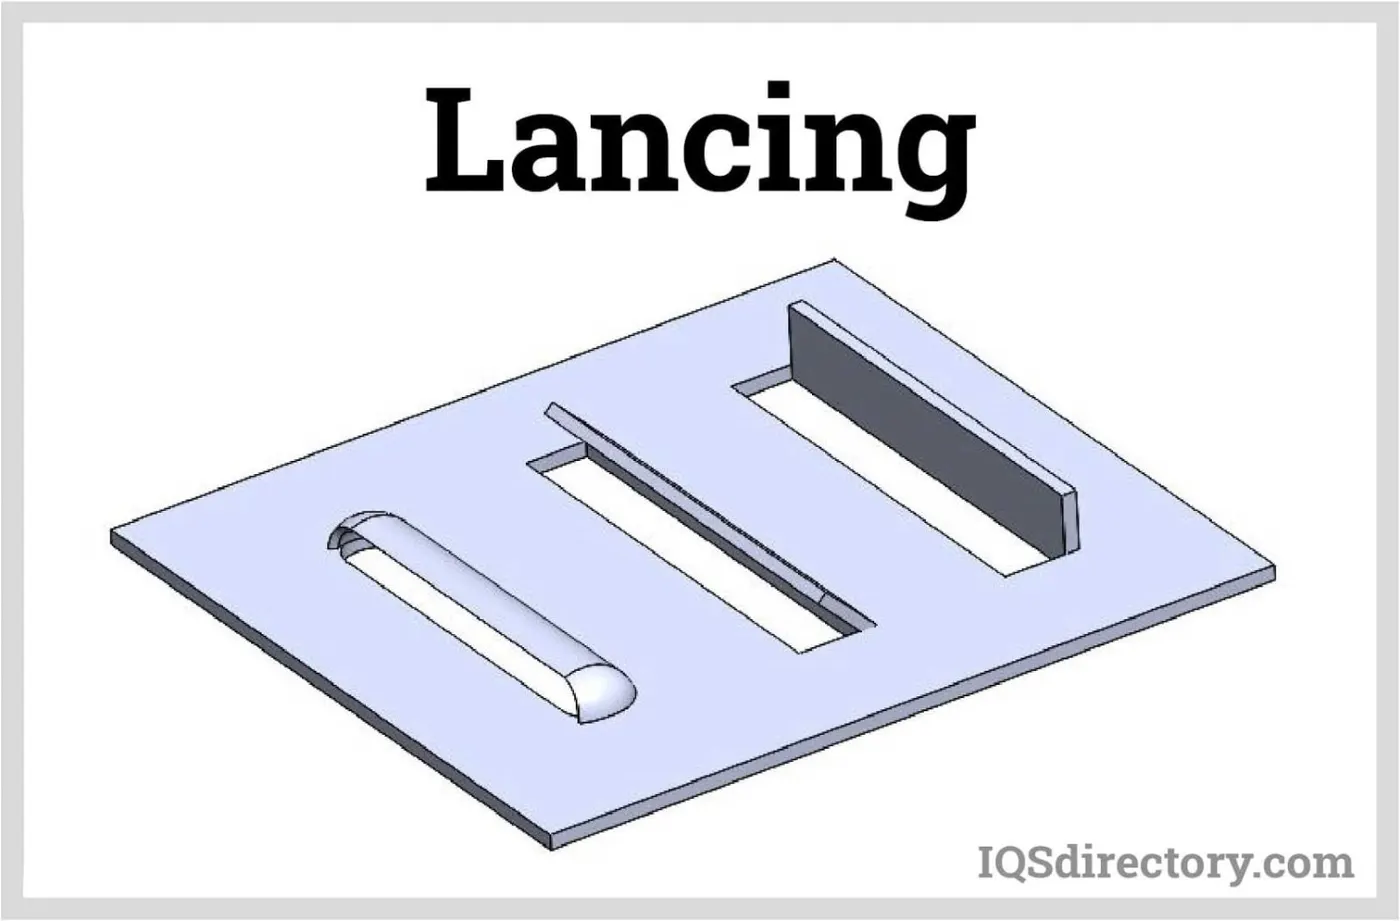
Lancing is a process in the sheet metal where the metal is cut to a sheet of metal through part of its length and then bending the cut portion. No material is removed in the lancing process. It is used to make tabs, vents, louvers in sheet metal workpiece. Here in back door inner panel, we use this operation
Hemming
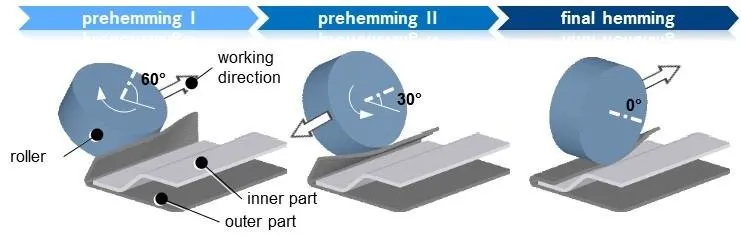
Hemming is a type of forming operation in manufacturing components. Here the edges of the sheet metal are folded on the other part achieving tight fit. This joins the both parts without affecting the appearance and hence it is used in hood, doors, fenders, tailgates etc. In tailgate it is used to join the inner and Outer panel of the tail gate.
There are various types of hemming operations
1 - Conventional Dai Hemming
2 - Roll Hemming
Conventional Dai Hemming
This is used for mass productions. Here a hemming tool is used to fold the entire length of the sheet metal. Depending on the opening angle that will be several steps of the Hemming process. But this is an expensive process and it is restricted to flat and complicated profiles cannot be made in hemming.
Roll hemming
The name says rollers are used in the hamming process and industrial robots are used to get the rollers over the part to fold over the other part and hemming is done. Comparing to the conventional die hemming the tool cost are significantly low the old hemming but the cycle time is higher the roll hemming
Spot Weld
Spot welding is a type of electric resistance welding. It is also known as resistance spot welding. The process of spot welding is sheet metals are made into contact with each other and pressure is applied on specified points. So, heat is generated from the resistance and weld is formed
Back Door Design Using NX-Cad
Inner panel
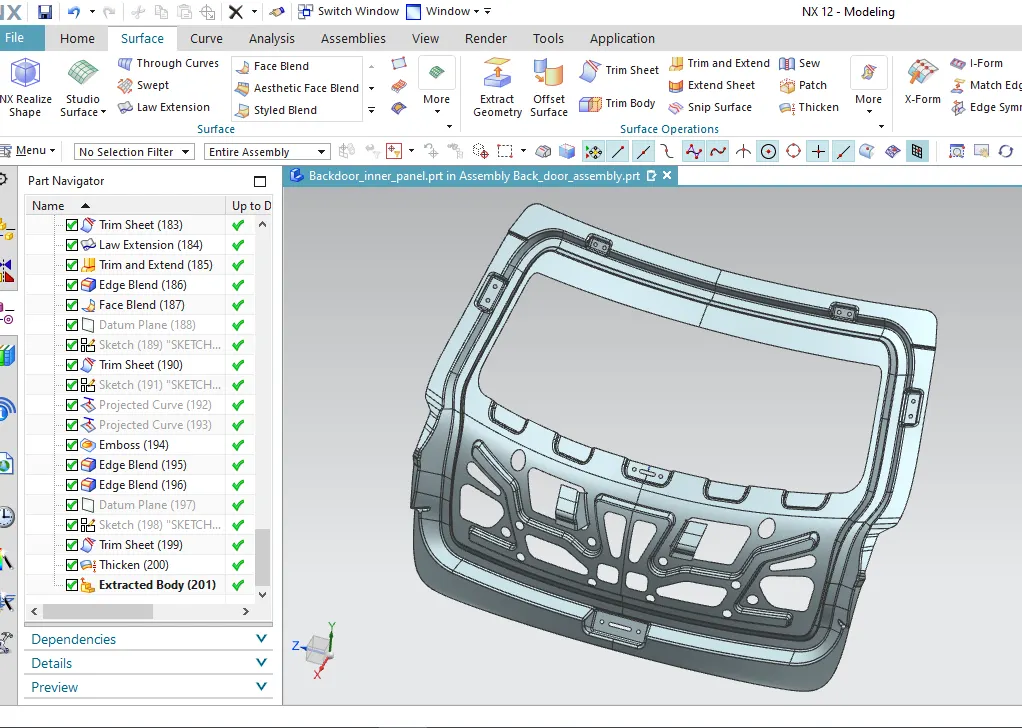
Back door has the mountings for hinges, gas stay, wiper motor, mastic area, striker and so on.
The block is stamped as single part. This reduces the cost and number of tools needed to manufacture.
This is the strengthening element of the back door. Inner panel is hemmed with outer panel finally. Aluminum or steel will be used for manufacturing the tail gate inner panel.
Reinforcements are added where ever needed. Thickness is given 0.75mm in the above model towards the outer panel. Flanges like Connecting flange, sealing flange and inner panel flange will be present in the inner panel.
Outer panel
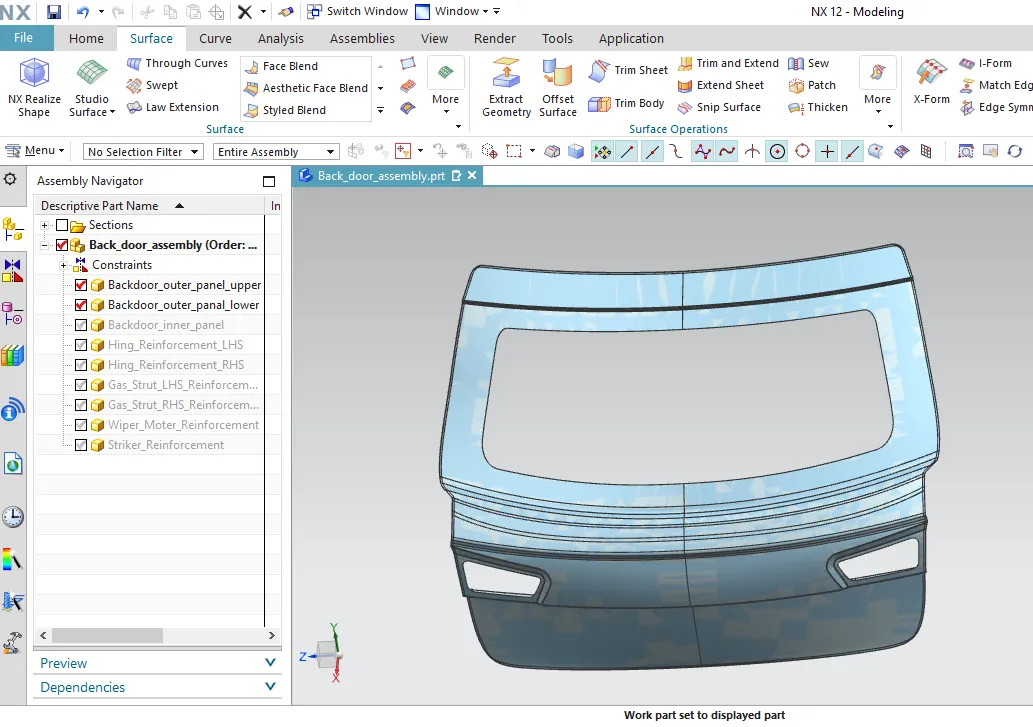
Outer panel is the aesthetic part of the tail gate. It will be attractive in look. coatings are given to keep it scratch and rust resistant.
The outer panel also has the provisions for the tail lamp, rear fog lamp and also has the provision for license plate mountings.
Most of the hatchback cars have the provision for wiper motor. Thickness is given 0.75mm in the above model towards the inner panel. Hemming is done to join the inner and outer panel.
Hinge Reinforcement
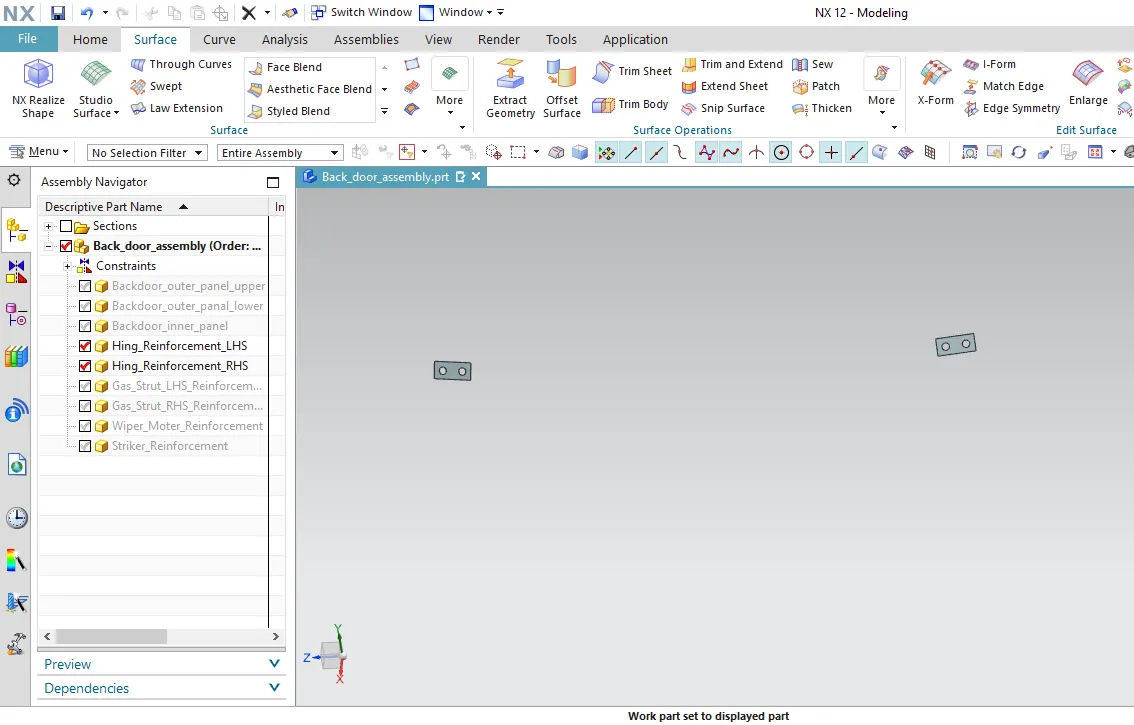
Hinges are used to opening and closing of the back door. Both halves of hinge on back door and roof combines to operate the door. Reinforcement is given to compensate the load acting on the region. Thickness is given 1.5mm in the above model towards the outer panel.
Gas Stay Reinforcement
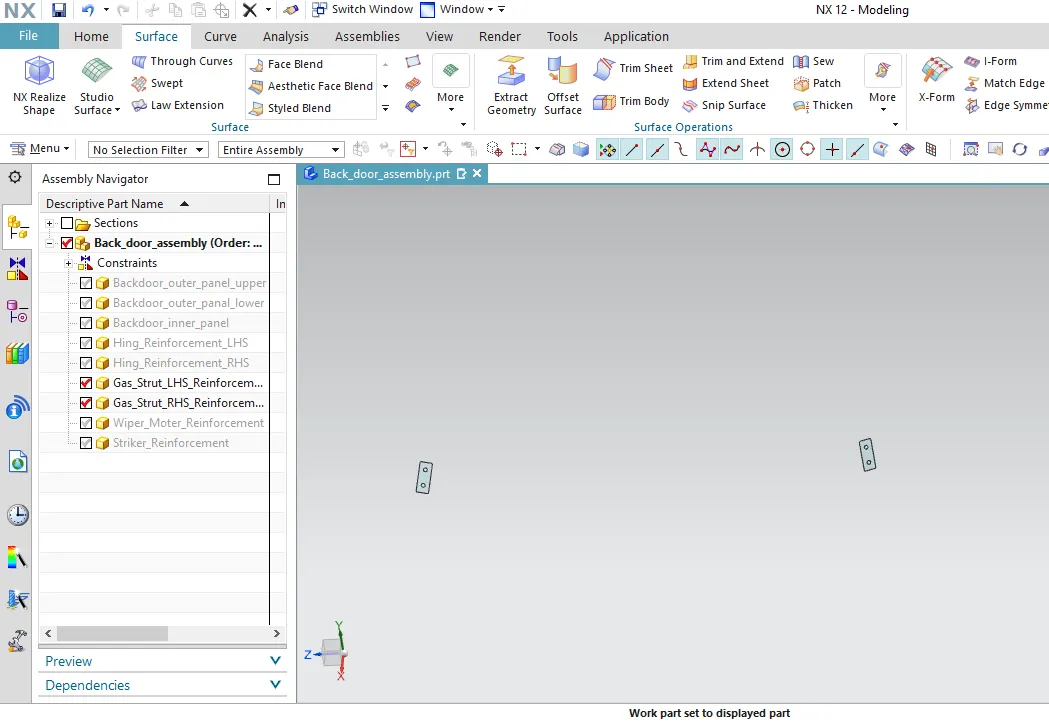
Gas stay in a tail gate is used hold open and close the tail gate. It eliminates man power by holding the back door open in position. one end of the gas stay is fixed on the door and other on the body side.
Wiper Motor Reinforcement
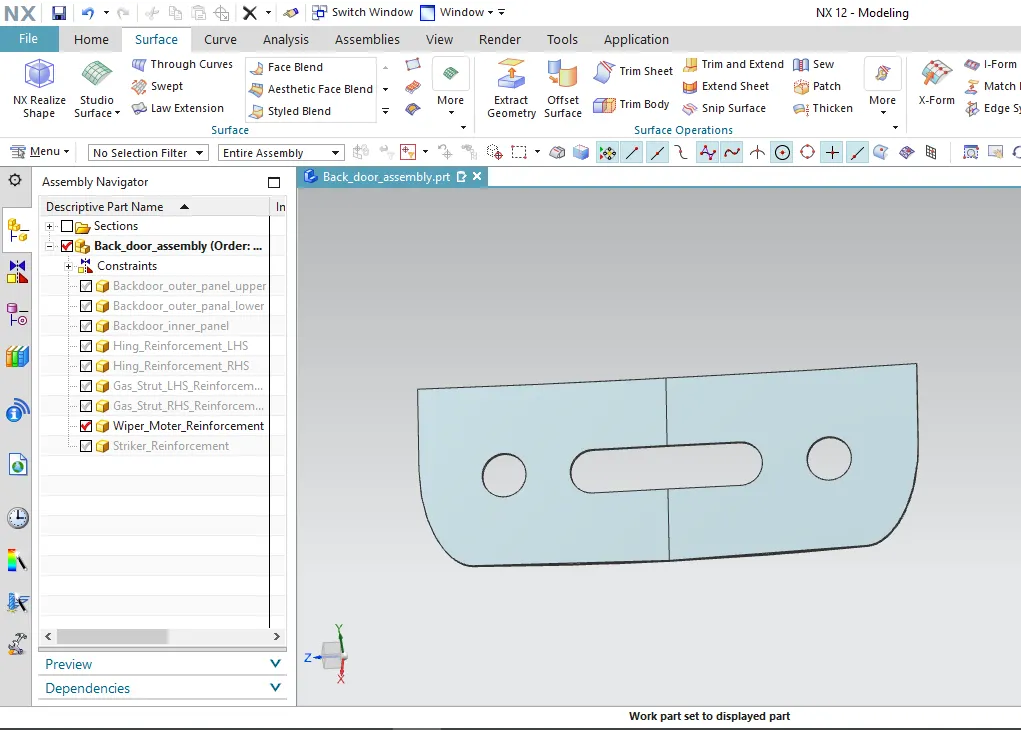
Wiper motor is placed in the back door area under the glass mounting portion. It comprises of small motor and modules that actuates the wiper. reinforcement is given to strengthen the part locally. here the thickness is given 1.5mm.
Striker Reinforcement
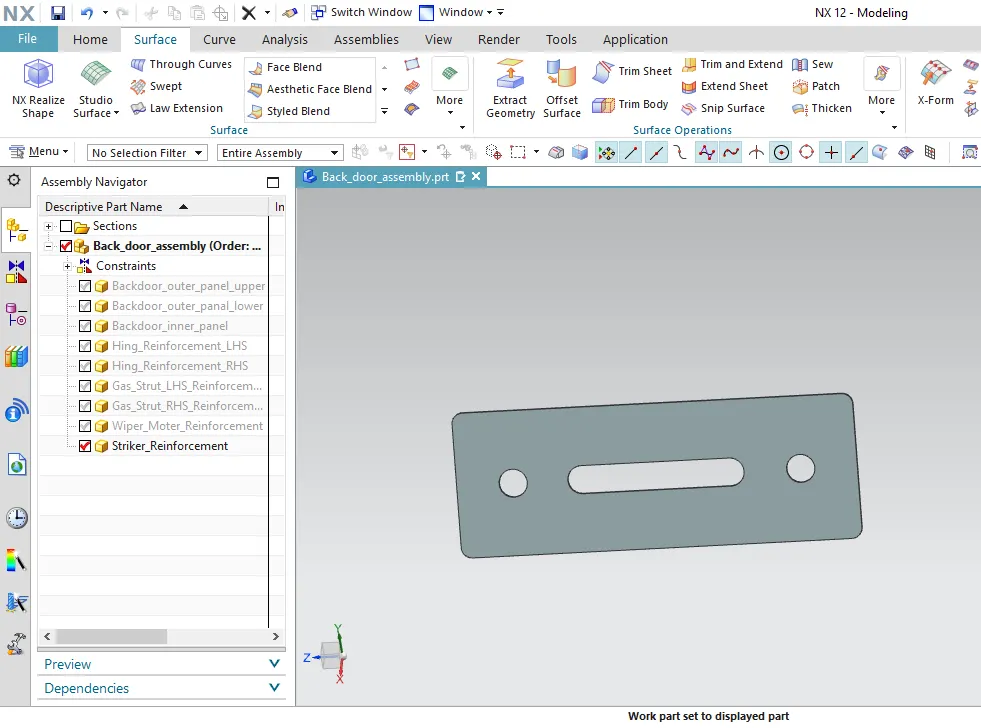
Latch and striker are responsible for locking of the back door. Stress will be developed as we frequently open and close the door so adding a reinforcement will make it stronger.
Draft Analysis
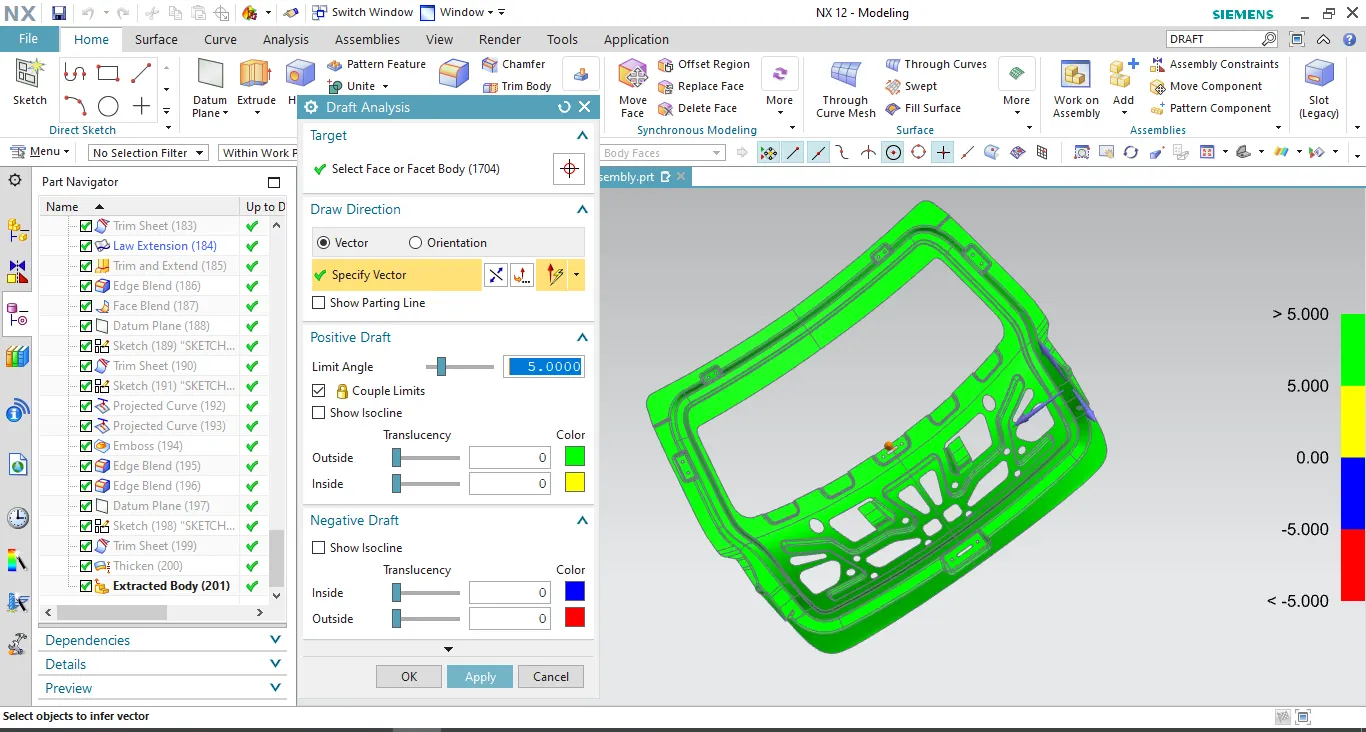
Here are the parts that are made as per the master section and also clearing the draft analysis. Draft analysis is done in NX software. We can change the draft angle and analyze is it clearing the required criteria. It is shown is different color zones. So, identifying it will be easier. It will let us know that the part can be removed easily during manufacturing or not. Minimum draft angle of 7 Degree is considered for analysis. green color infers on the parts that all face along the tooling direction has positive draft angle greater than 7 degree and passed in analysis.
Hemming
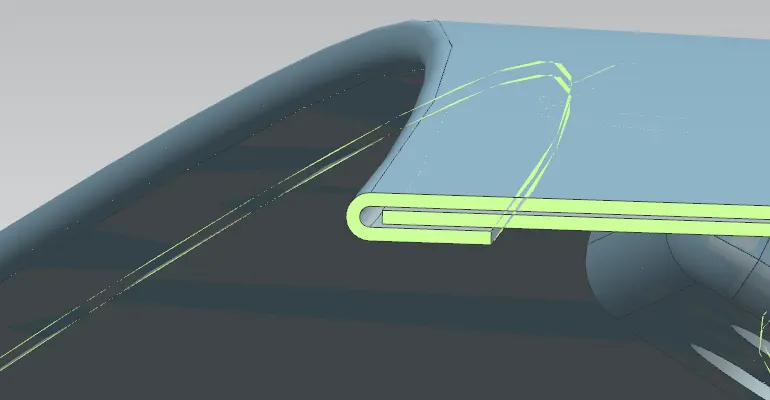
As explained above about the hemming. Here we have used it to join the inner and outer panel of the back door.
Hemming relief
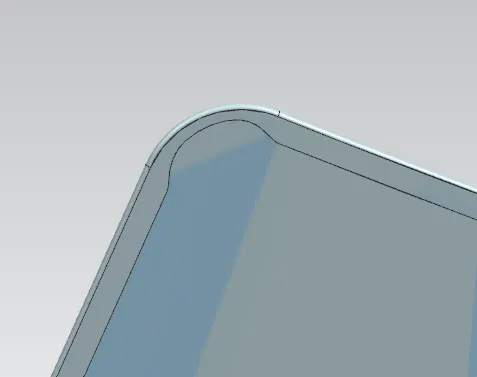
While we do hemming, we give corner relief at the turns of the part. because during manufacturing rolls cannot travel at the corner and it may create wrinkles while hemming at the corner. so, we give a curvature for avoiding those problem.
Lancing
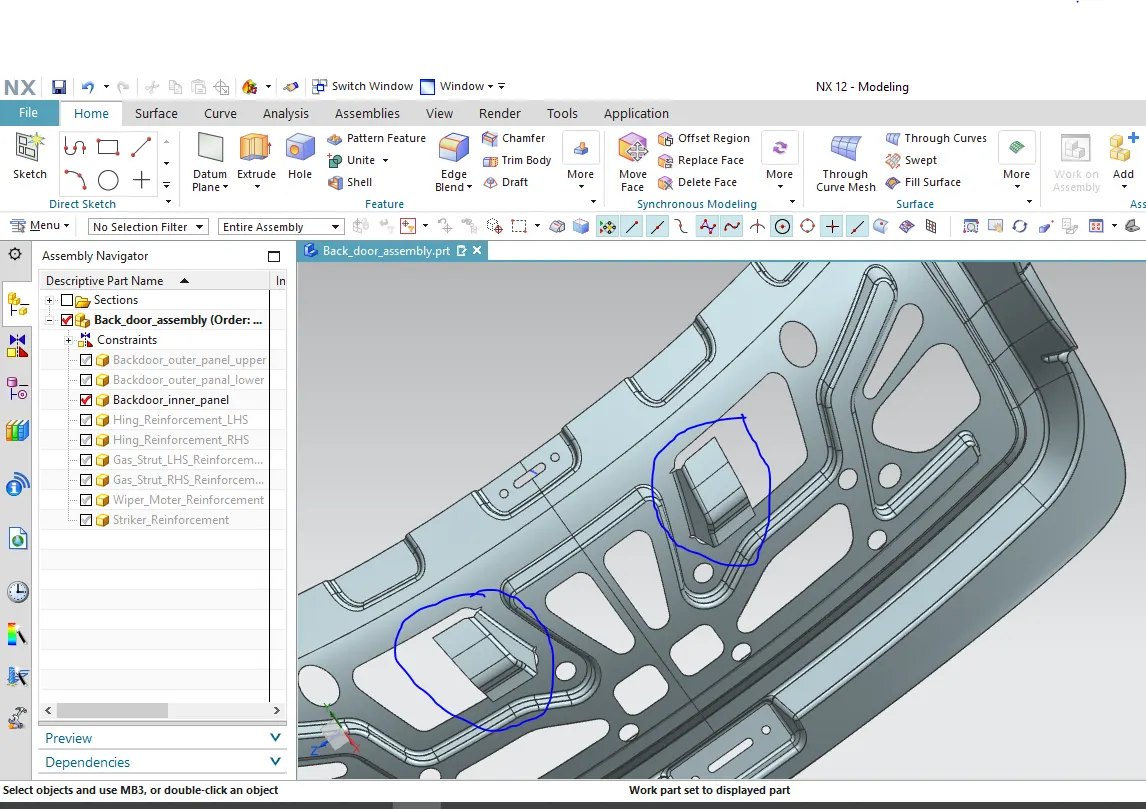
As mentioned above about the lancing process. Here we use in the inner panel of the door. It is done to join the outer and inner panel with the help of mastic sealants.
Latch Positioning
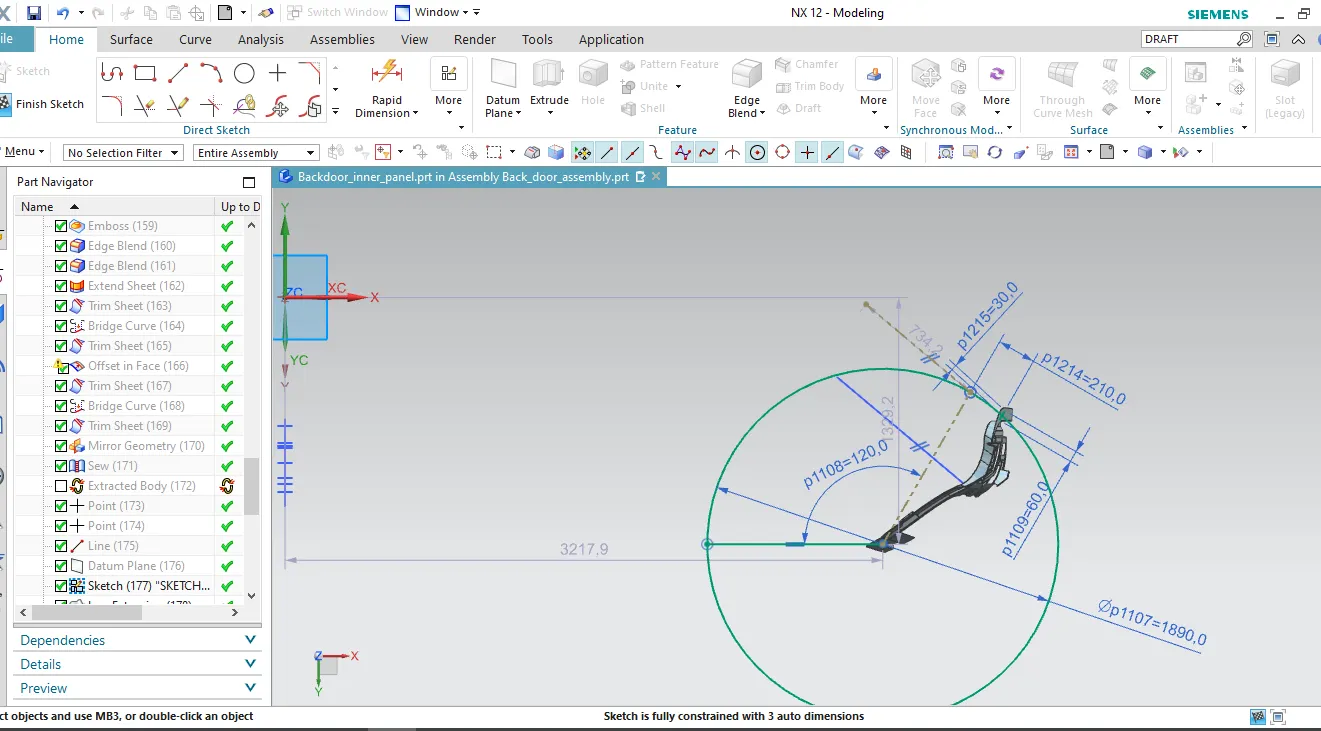
Latch and striker should be perpendicular to the hinge so only it will open and close properly. So, I have made this trajectory to position the striker emboss.
Conclusion
We have designed the back door by the provided styling surface. By using appropriate design methods and provided the necessary reinforcements and embosses for the Back door design.