Simulation of Cyclone separator with Discrete Phase Modelling
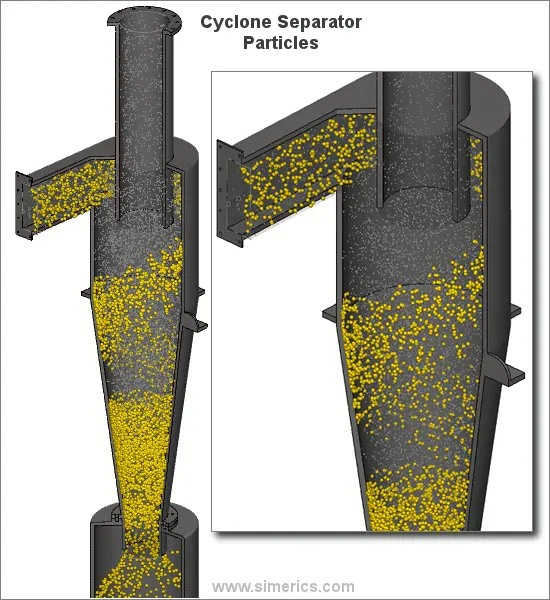
It is important to note that cyclones can vary drastically in their size. The size of the cyclone depends largely on how much flue gas must be filtered, thus larger operations tend to need larger cyclones. For example, several different models of one cyclone type can exist, and the sizes can range from a relatively small 1.2-1.5 meters tall (about 4-5 feet) to around 9 meters (30 feet)—which is about as tall as a three-story building!.
How it works
Cyclone separators work much like a centrifuge, but with a continuous feed of dirty air. In a cyclone separator, dirty flue gas is fed into a chamber. The inside of the chamber creates a spiral vortex, similar to a tornado. The lighter components of this gas have less inertia, so it is easier for them to be influenced by the vortex and travel up it. Contrarily, larger components of particulate matter have more inertia and are not as easily influenced by the vortex.
Since these larger particles have difficulty following the high-speed spiral motion of the gas and the vortex, the particles hit the inside walls of the container and drop down into a collection hopper. These chambers are shaped like an upside-down cone to promote the collection of these particles at the bottom of the container. The cleaned flue gas escapes out the top of the chamber.
Most cyclones are built to control and remove particulate matter that is larger than 10 micrometers in diameter. However, there do exist high-efficiency cyclones that are designed to be effective on particles as small as 2.5 micrometers. As well, these separators are not effective on extremely large particulate matter. For particulates around 200 micrometers in size, gravity settling chambers or momentum separators are a better option.
Out of all of the particulate-control devices, cyclone separators are among the least expensive. They are often used as a pre-treatment before the flue gas enters more effective pollution control devices. Therefore, cyclone separators can be seen as "rough separators" before the flue gas reaches the fine filtration stages.
Effectiveness
Cyclone separators are generally able to remove somewhere between 50-99% of all particulate matter in the flue gas. How well the cyclone separators are actually able to remove this matter depends largely on particle size. If there is a large amount of lighter particulate matter, fewer of these par0ticles are able to be separated out. Because of this, cyclone separators work best on flue gases that contain large amounts of big particulate matter.
There are several advantages and disadvantages to using cyclone separators. First, cyclone separators are beneficial because they are not expensive to install or maintain, and they have no moving parts. This keeps maintenance and operating costs low. Second, the removed particulate matter is collected when dry, which makes it easier to dispose of. Finally, these units take up very little space. Although effective, there are also disadvantages in using cyclone separators. Mainly because the standard models are not able to collect particulate matter that is smaller than 10 micrometers effectively and the machines are unable to handle sticky or tacky materials well.
Empirical models used to calculate the cyclone separator efficiency
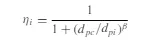
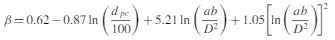
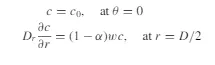
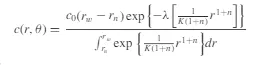
Where,
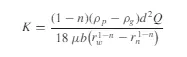 and,
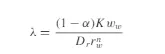
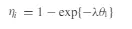
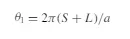
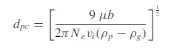
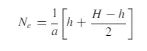
Model Set up
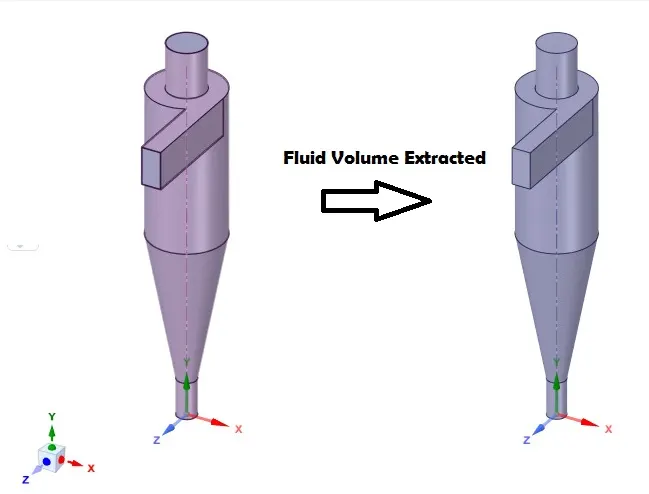
Model
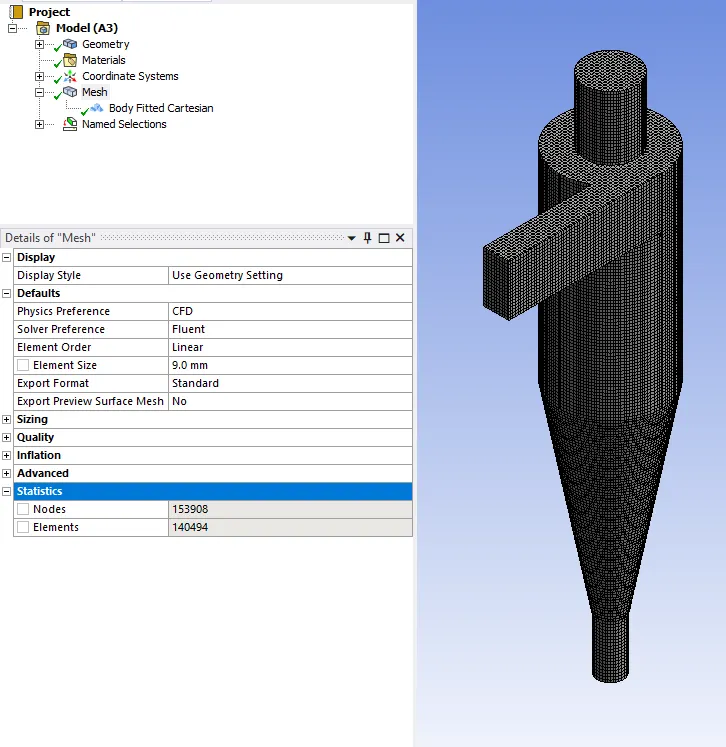
Mesh
Global mesh size 9mm
Body fitted cartesian element size 5.2623mm
Total no of elements - 140494
Nodes - 153908
Solver and Turbulence model
Turbulance model - Kepsilon/RNS/swirl dominated flow
solver - steady-state/pressure based with gravity acting on the y-axis (-9.81)
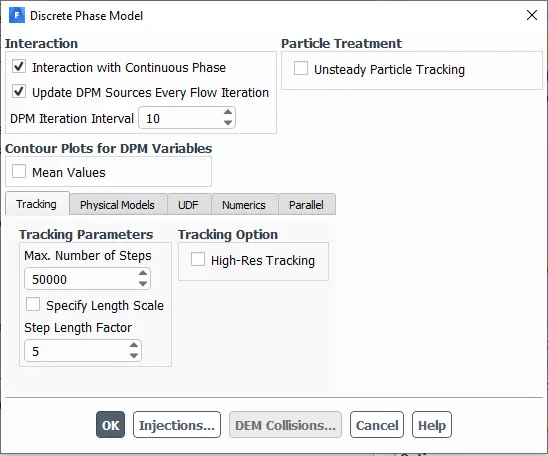
Discrete phase model
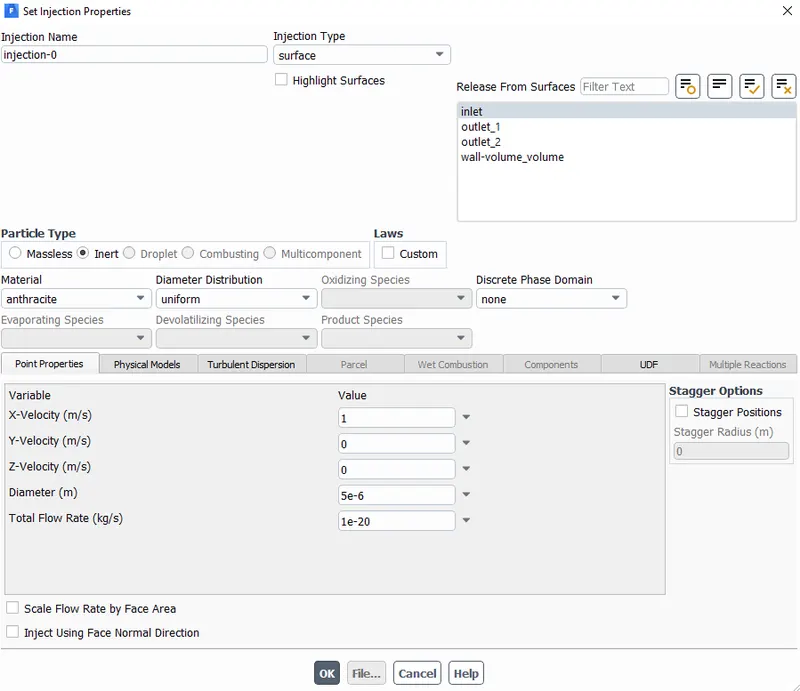
Injections
Boundary Conditions
Inlet and wall:- Reflect
Outlet(Top):- Escape
Outlet(Bottom/dustbin) - Trap
Number of iteration 1000
Part 1
The velocity of particle kept constant at 3m/s and particle size is varied
Case 1
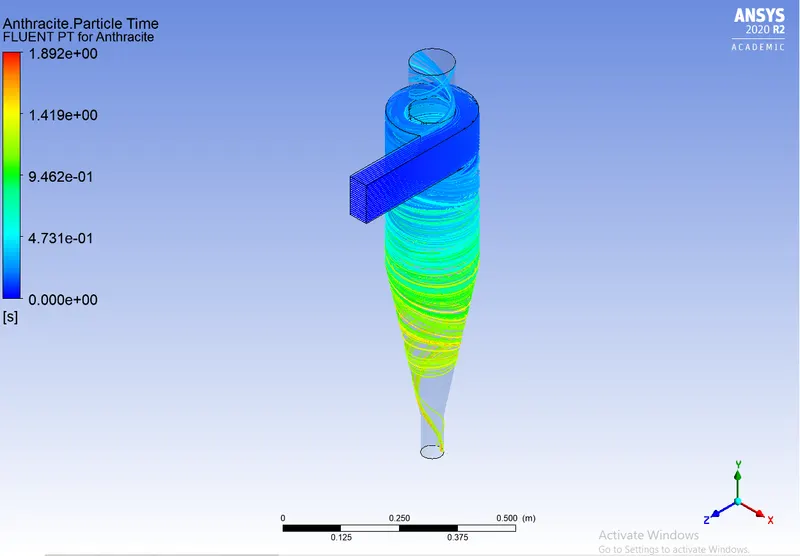
Particle size 5e-6m
Residual
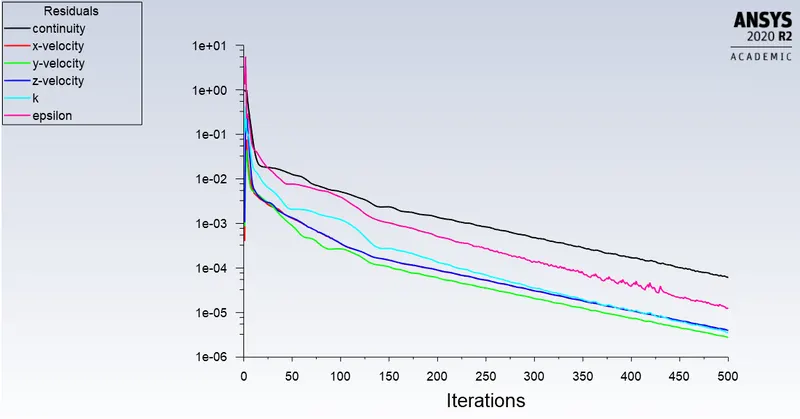
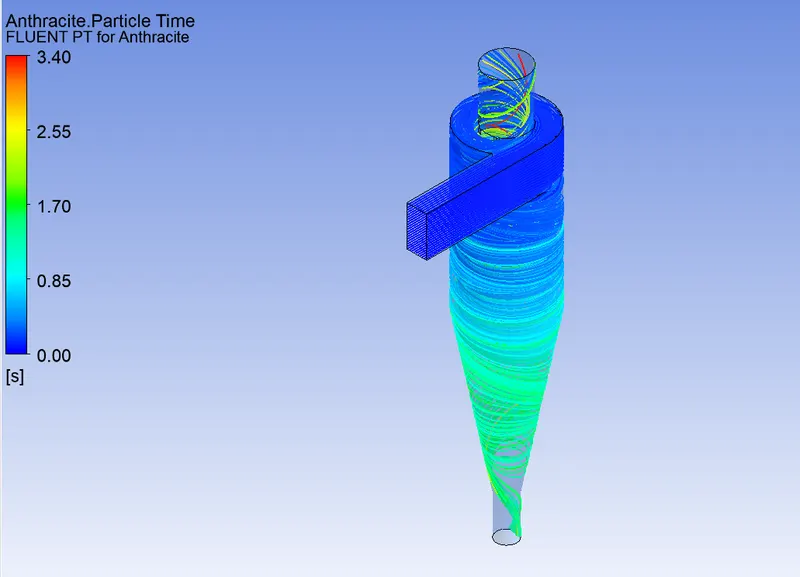
Anthracite Particle time
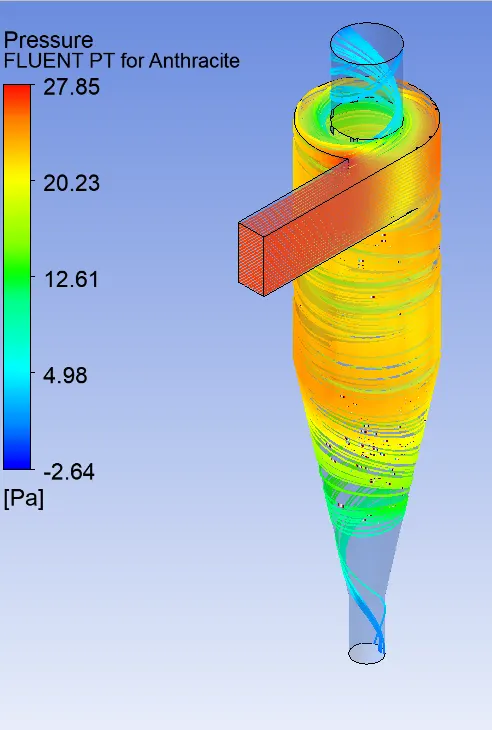
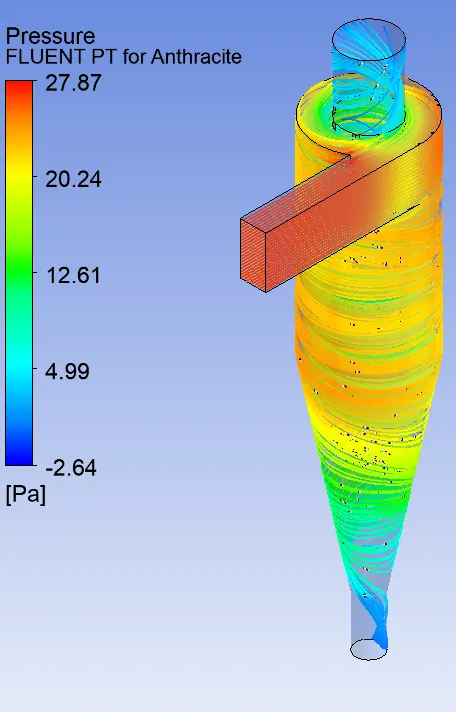
Pressure Drop
Case 2
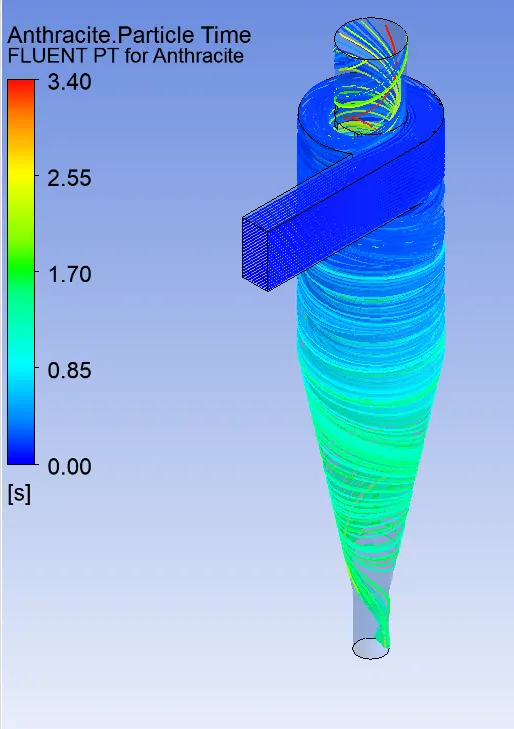
Particle size 3e-6m
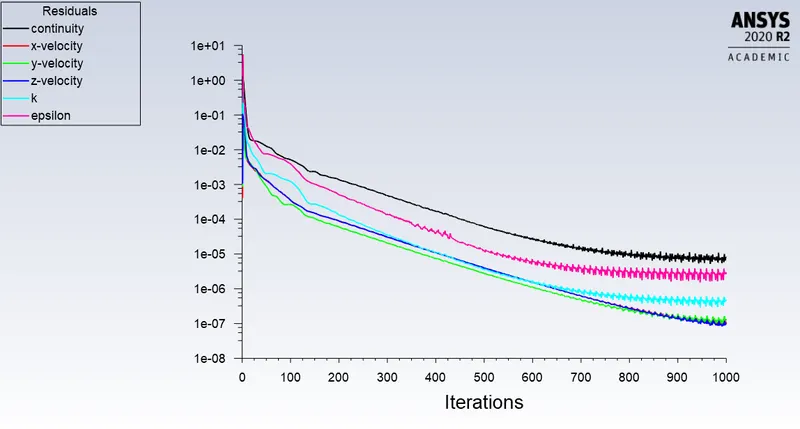
Residual
Anthracite Particle time
Pressure drop
Case 3
Particle size 1m/s
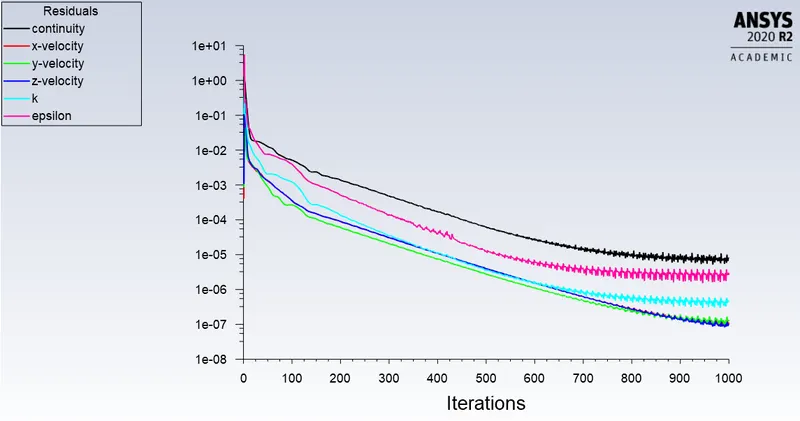
Residual
Anthracite Particle time
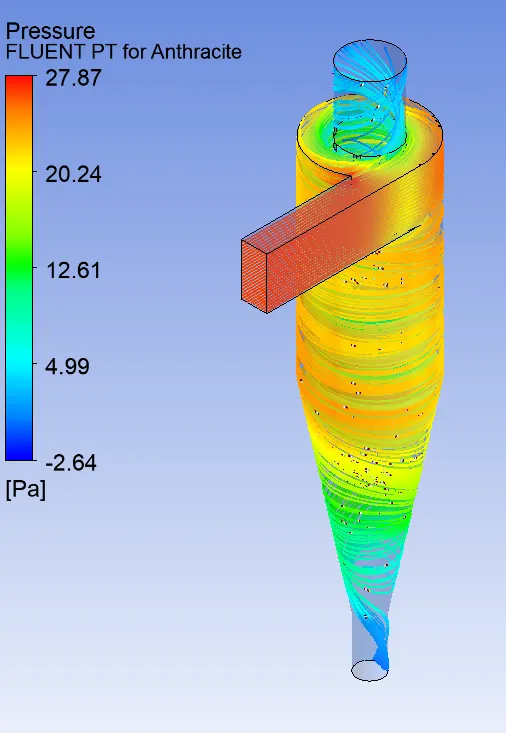
Pressure drop
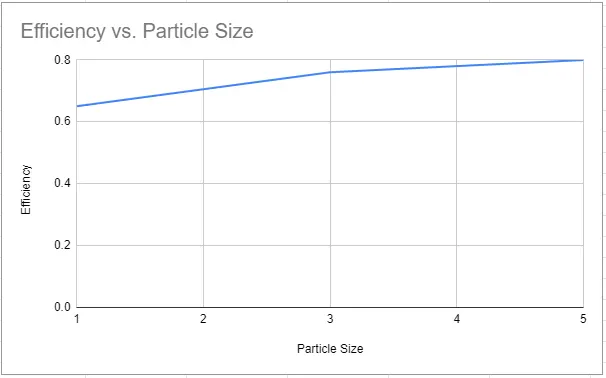
Tabulation
| Particle Size | 5e-6 | 3e-6 | 1e-6 |
| Number tracked | 190 | 190 | 190 |
| Trapped | 153 | 145 | 124 |
| Escaped | 37 | 45 | 63 |
| Incomplete | 0 | 0 | 3 |
| Efficiency | 0.80 | 0.76 | 0.65 |
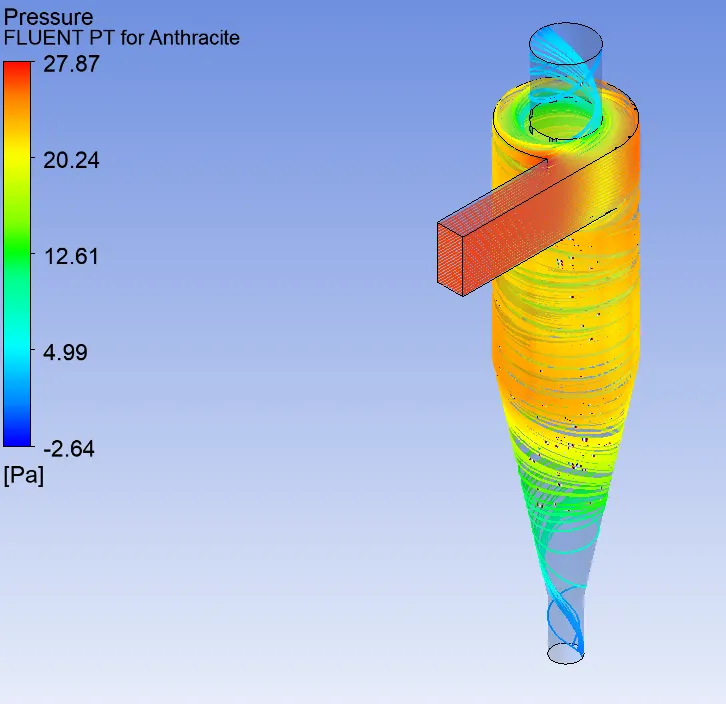
Pressure Drop = 28.87-2.64 = 25.23 Pa
Part 2
Keeping Particle size constant at 5e-6m and changing velocities of particle and continuous flow
Case 1
Velocity of Particle and Continuous-flow = 5 m/s
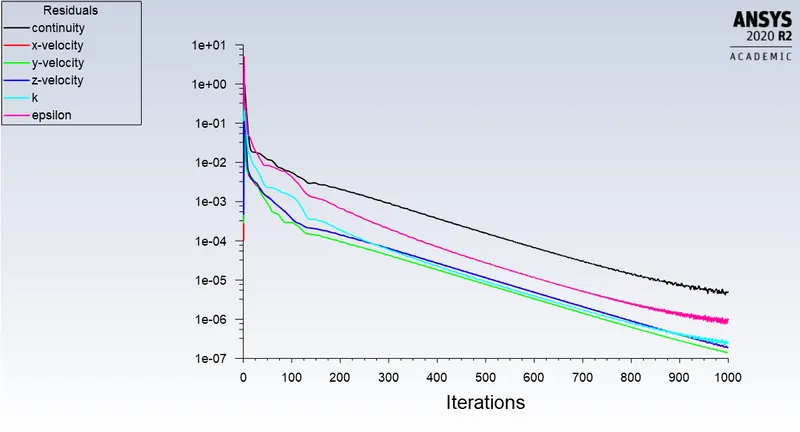
Residual
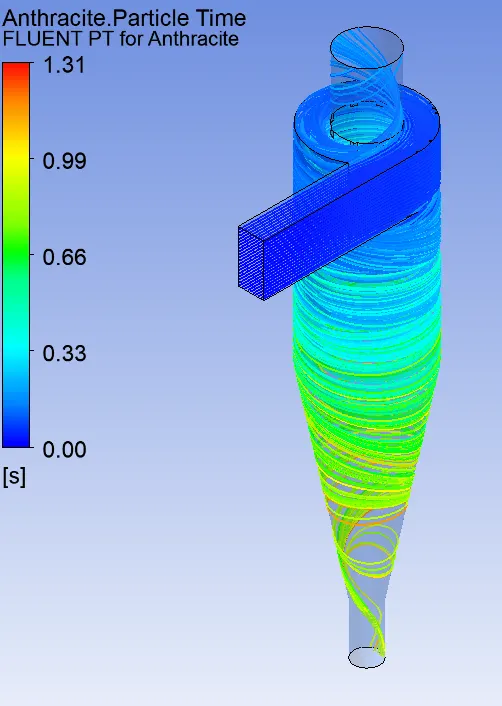
Anthracite Particle time
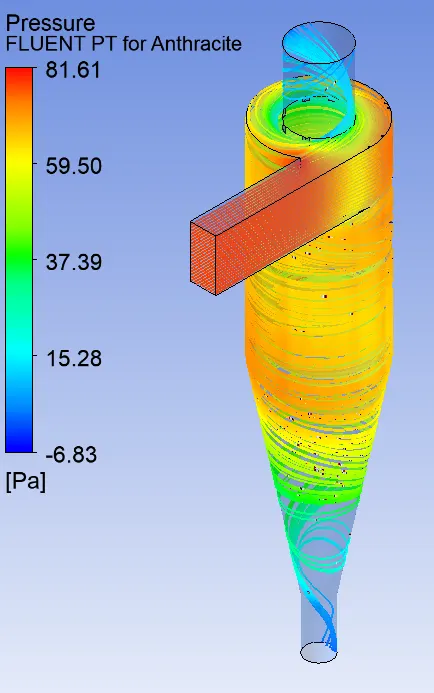
Pressure Drop
Case 2
Velocity of Particle and Continuous-flow = 3 m/s
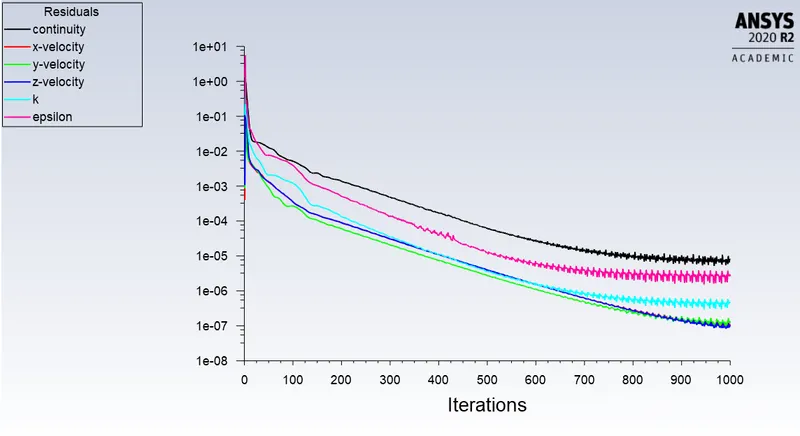
Residual
Anthracite Particle Time
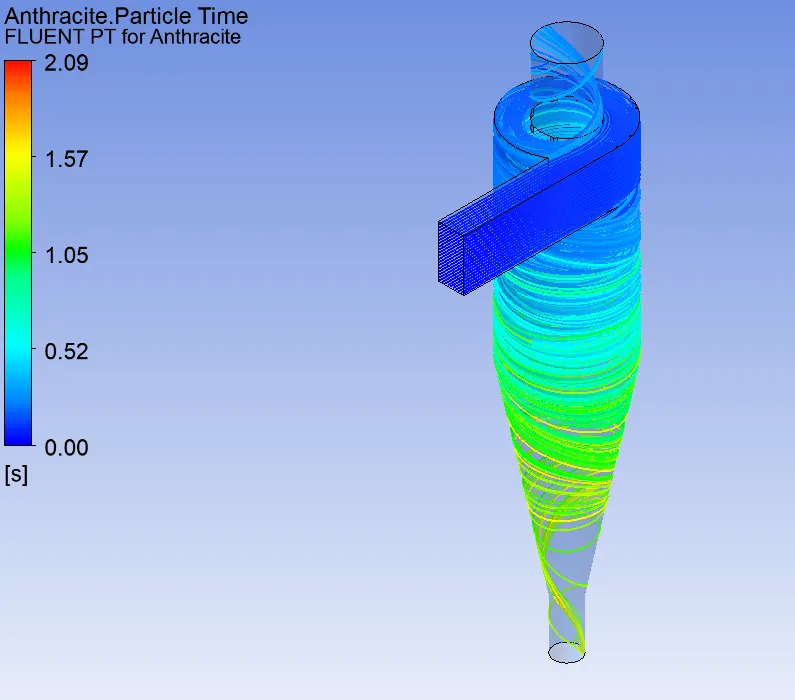
Pressure Drop
Case 3
Velocity of Particle and Continuous-flow = 1 m/s
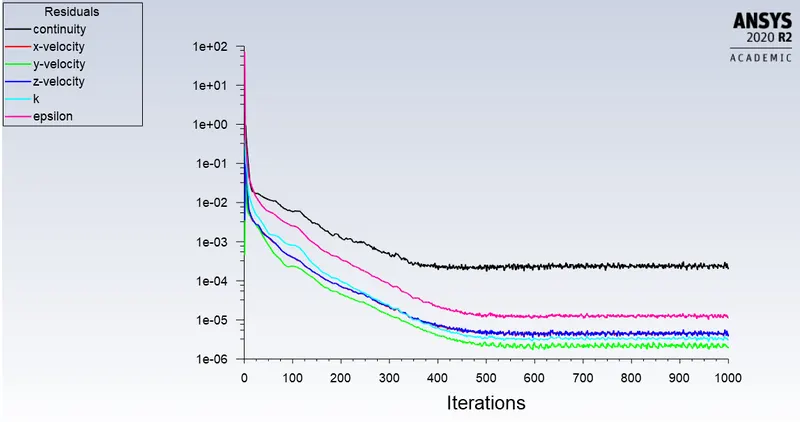
Residual
Anthracite Particle Time
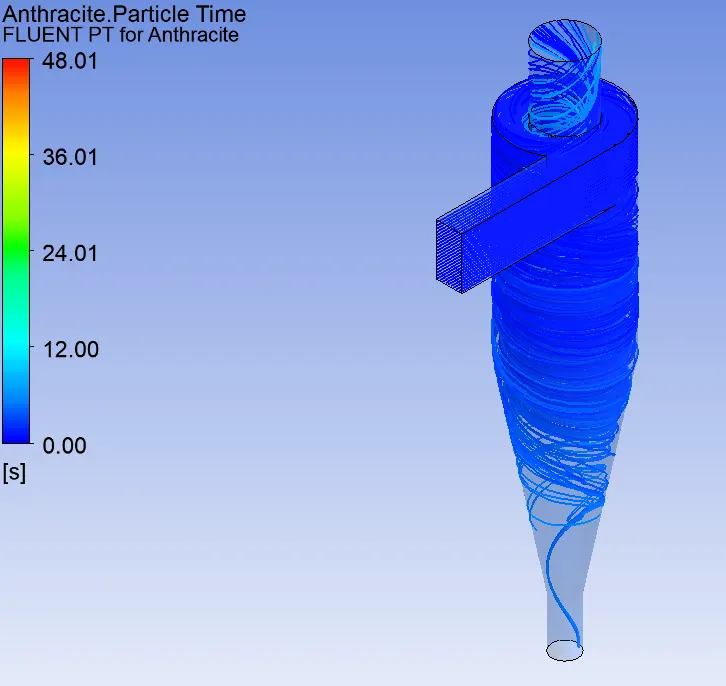
Pressure Drop
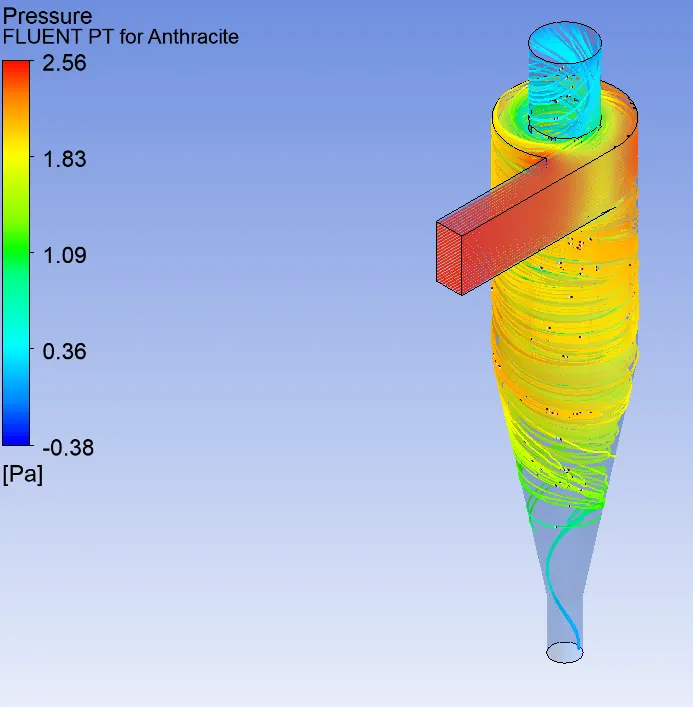
Tabulation
| Velocity in m/s | 5 | 3 | 1 |
| Number Tracked | 190 | 190 | 190 |
| Trapped | 156 | 154 | 26 |
| Escaped | 34 | 36 | 48 |
| Incomplete | 0 | 0 | 112 |
| Efficiency | 0.82 | 0.81 | 0.13 |
videos of Simulations
Part 1
Part 2
Conclusions:
Continuous Flow and particle velocity kept constant 3m/s
Particle size kept constant 5e-6m
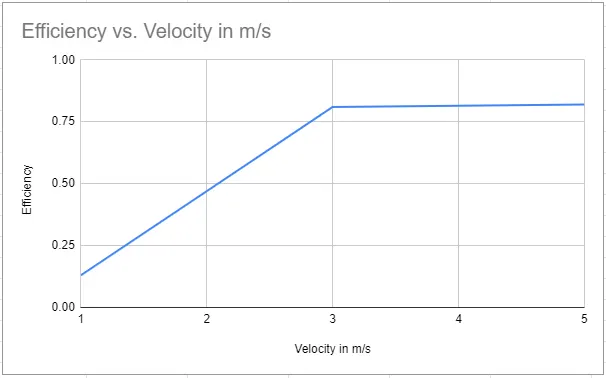
The most important economical parameters of a cyclone separator are separation efficiency and pressure drop. Generally, the increase of gas inlet velocity will increase the separation efficiency, but it will also increase the pressure drop. This is supported by the above graphs and tabulation.
The pressure drop across the cyclone is of much importance in a cyclone separator. The pressure drop significantly affects the performance parameters of a cyclone. The total pressure drop in a cyclone will be due to the entry and exit losses, and friction and kinetic energy losses in the cyclone. Pressure drop increases with the inlet gas velocity, efficiency can be enhanced with the increase of inlet gas velocity.