Week 8 - Challenge 5 - Core & Cavity Design
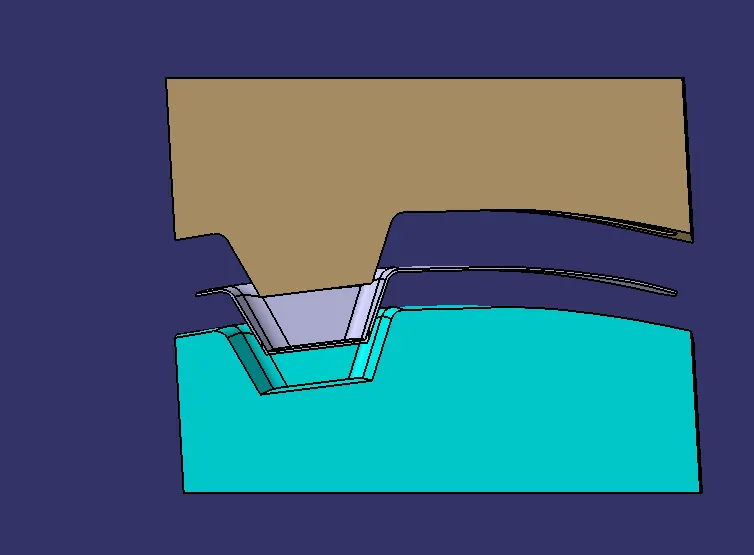
AIM - To create the core and cavity block for the switch bezel
INTRODUCTION
The Draft Analysis command enables you to detect if the part you drafted will be easily removed. This type of analysis is performed based on colour ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
Tooling direction is the main consideration for plastic part and mould parts because it defines the movement of the mould part and the possibility of the plastic part coming out from the mould part (Core and Cavity).
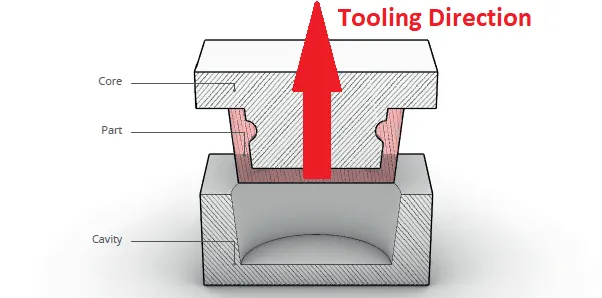
TOOLING DIRECTION
The Tooling Direction is basically the direction that the mold pulls apart. The mold is built in two separate pieces, basically. You have a Cavity side and you have the Core side. The Core pulls apart from the Cavity and that's the Dyeline or the Tooling Direction.
PROCEDURE FOR CREATING TOOLING AXIS
Firstly import the given class A surface to the catia.
- Check For any defects in the surface such as boundries and estimate the possible tooling direction
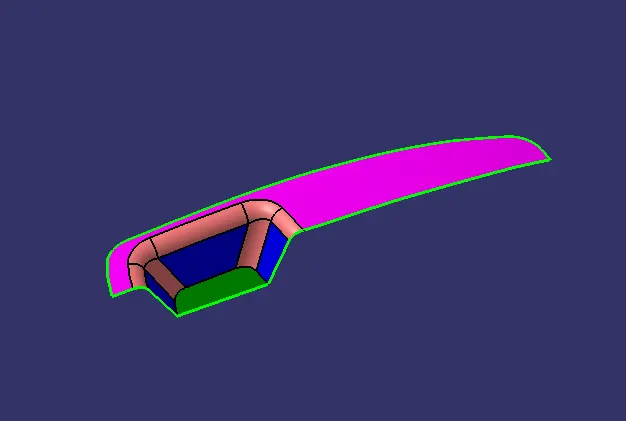
Create an intersection curve between Class A and X-axis and create a bisecting line between the lines of draft surface
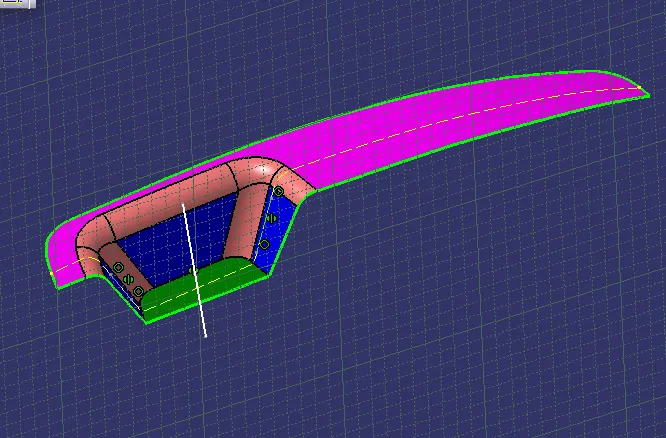
Create Y axis clearance with an angle to the draft surface
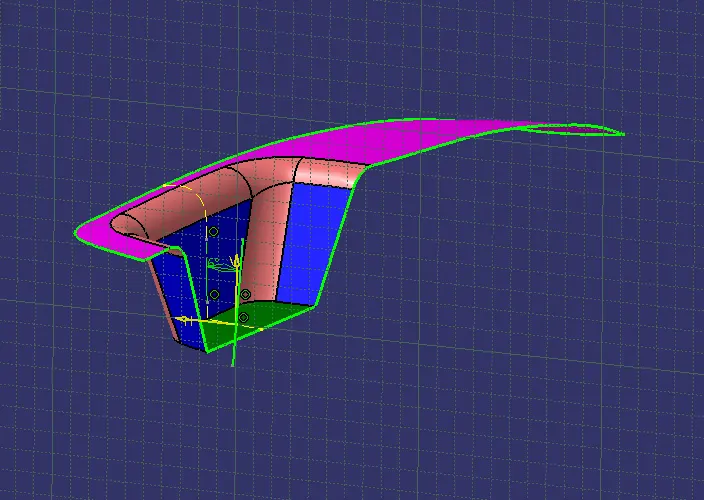
Create the actual Tooling axis by bisecting X and Y axis clearance lines
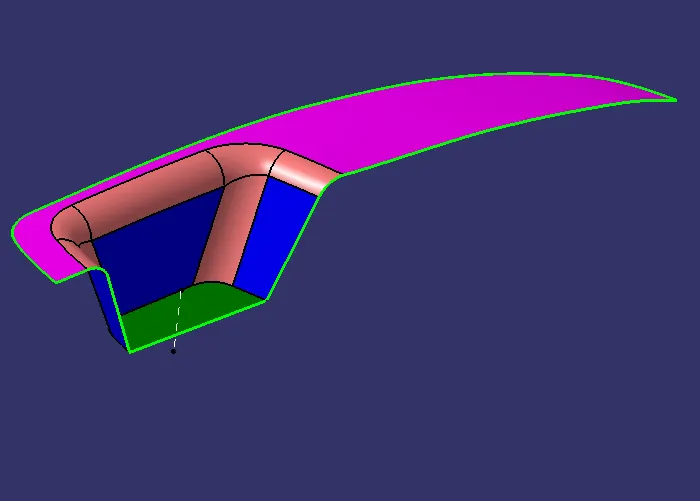
Draft Analysis
Using the feature draft analysis, perform draft analysis on the surface considering the tooling axis
3 degrees draft is optimum for the plastic moulding component
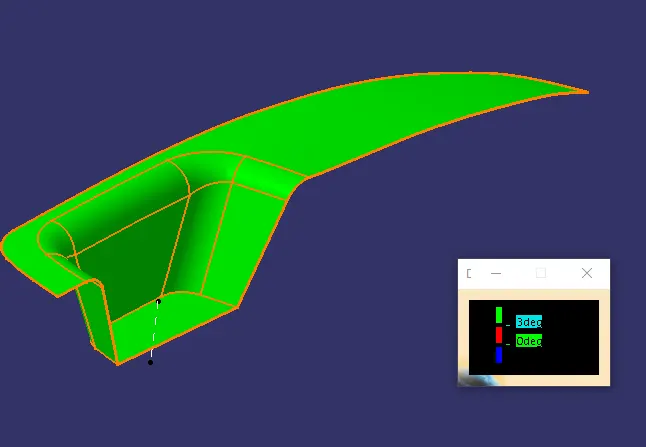
draft for A surface of switch bezel
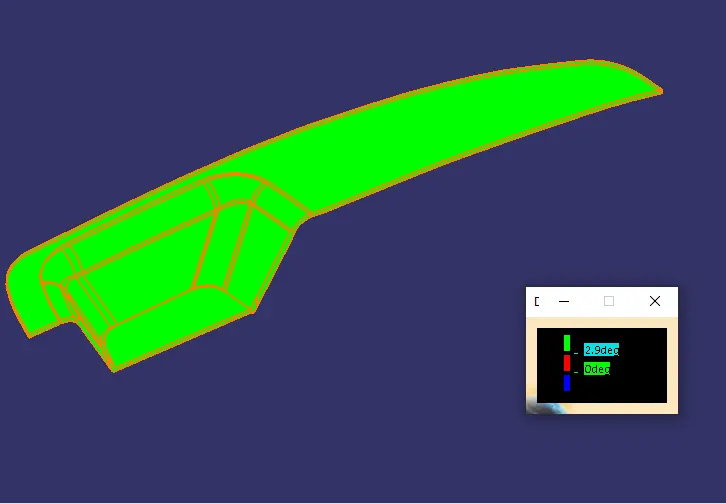
Drawft analysis for the switch bezel part
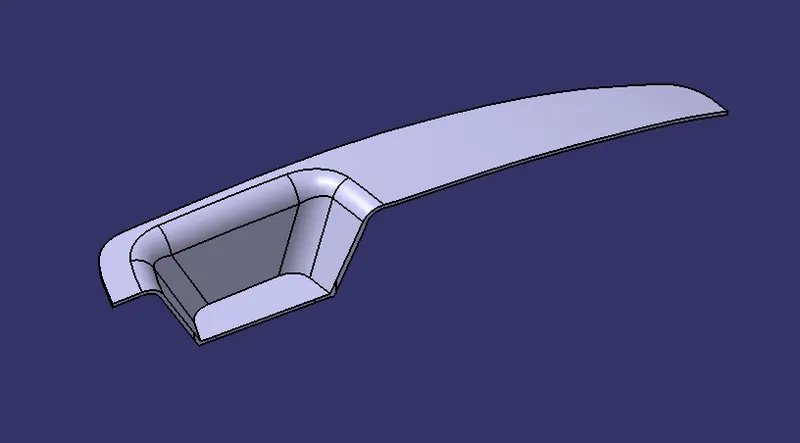
Switch bezel part
Creation of Core and Cavity blocks
Parting surface:Parting Surface Designed for the removal of the plastic product and the cold slug, the parting surface is where the core meets the cavity, and usually locates at the largest section of a product.
When designing a plastic injection mold, the selection of the parting surface is an important design factor. With a reasonable parting surface selection, the mold structure can be simpler, making it easier to mold and release the plastic product, with product quality guaranteed. If the parting surface is inappropriately selected, mold structure becomes complex, making it difficult to mold the plastic product, thus affecting product quality. Therefore, the selection of the parting surface is of great importance to the design of mold structure.
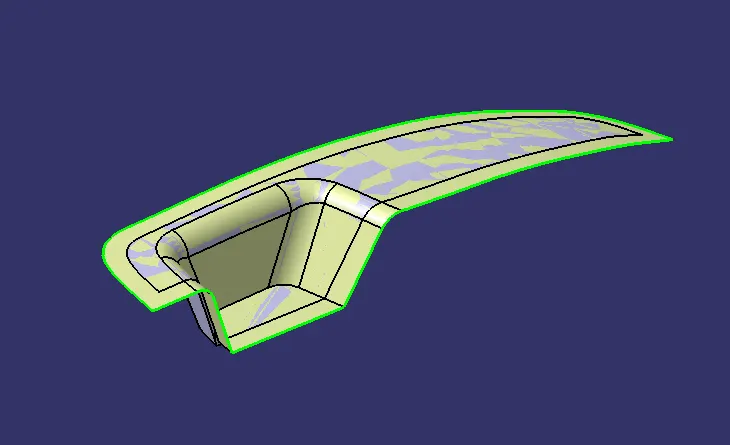
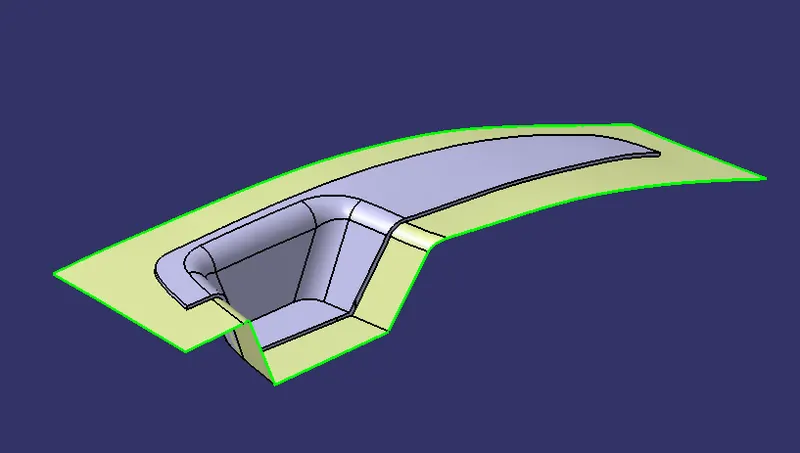
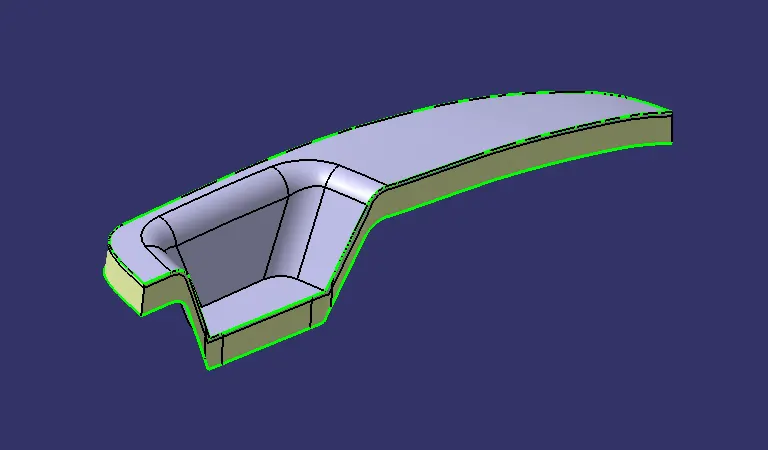
A,B,C surfaces are extracted and trimmed
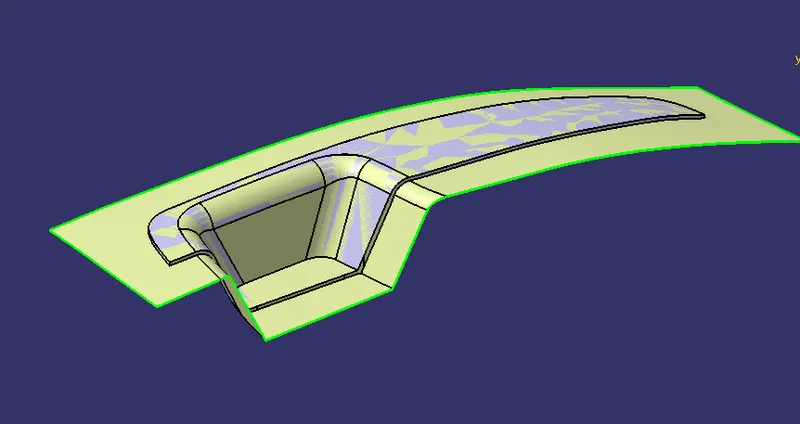
This surface is splited with parting line to create actual parting surface
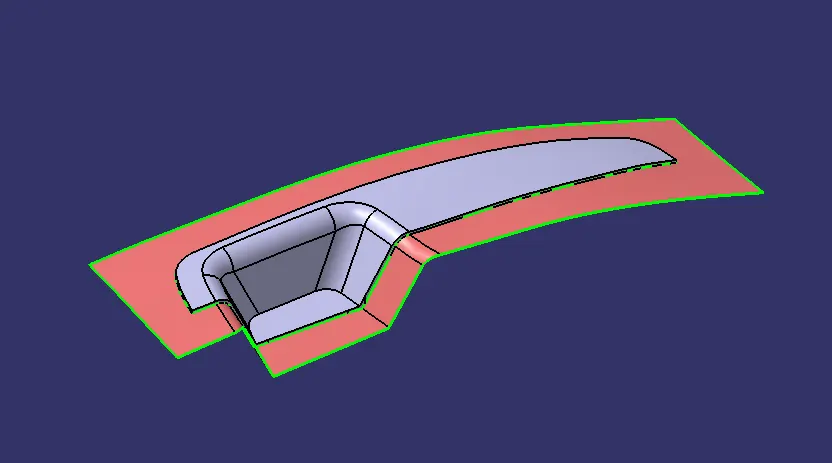
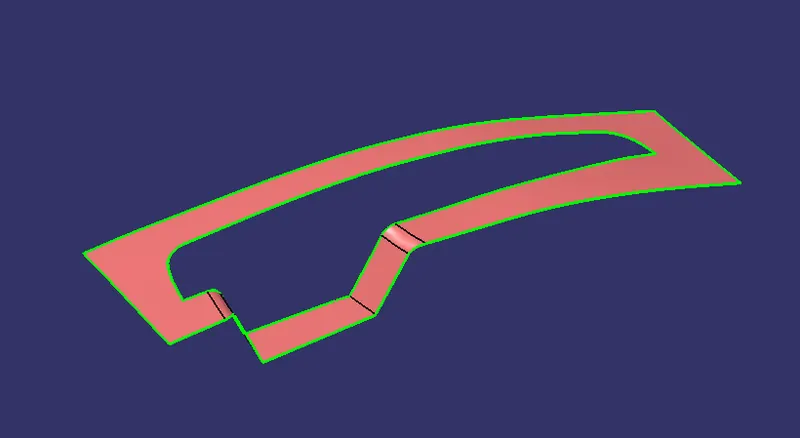
Parting line:A parting line, in industrial casting of molds, is the border line in which draft angles change direction. That is, it is the dividing line that splits the core and cavity halves of a molded part.
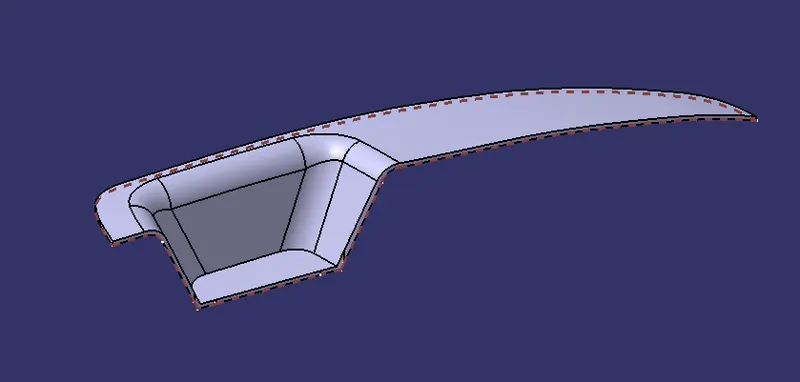
CORE DESIGN
Core - Cores are normally designed on the moving half of the mold base. This is the ejection side. On this side of the mold, there is the ejection system of the injection molding machine. This system connects to the ejector system of the mold. The core has the projection.
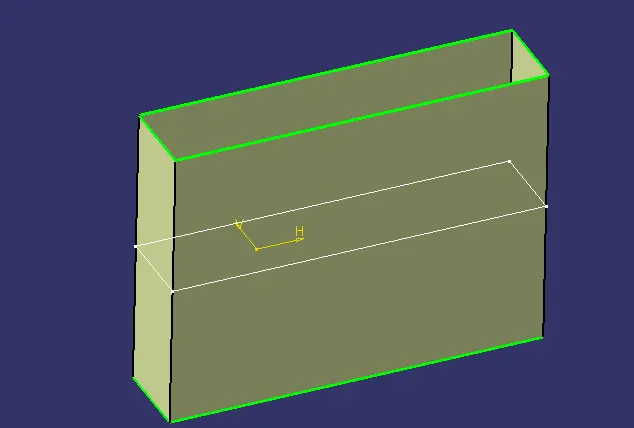
For creating core a rectangle is extruded which fits the actual part
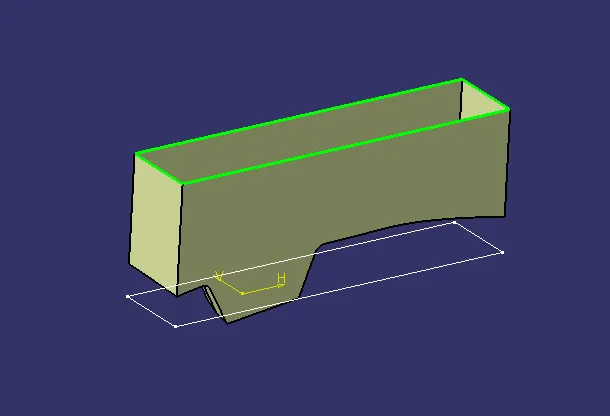
It is then trimmed with parting surface with part area
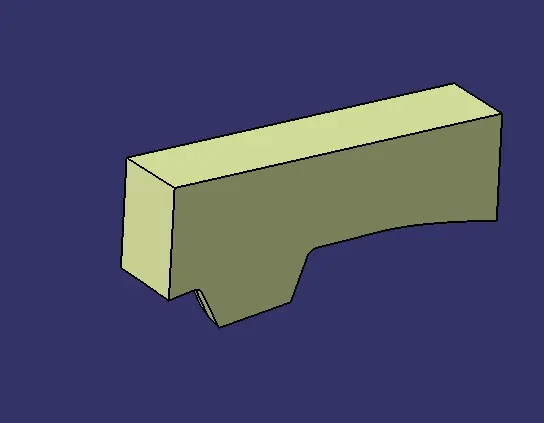
Finally it's top is filled and join together
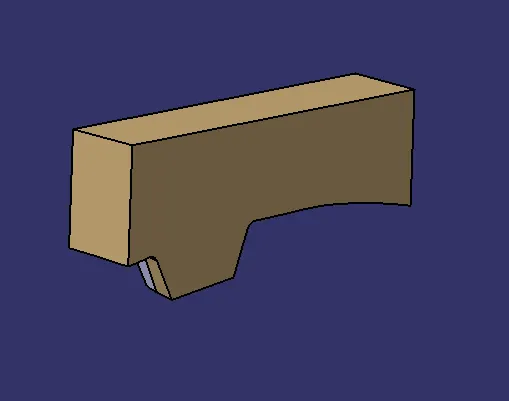
cavity - Cavities are normally designed in the fixed half of the mold base, the injection site. Sometimes, however, cavities may be mounted on the moving side. The cavity has depression. Cavities are normally the "nice side" of the plastic part: well finished, without marks.
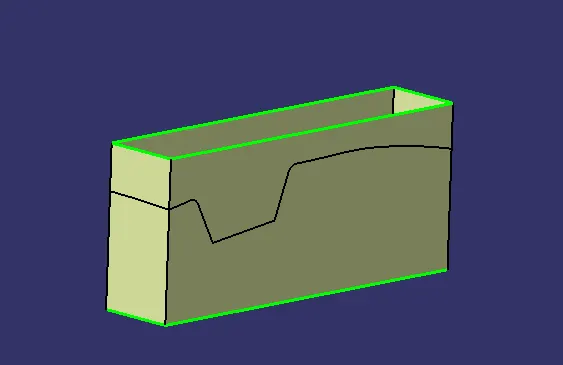
Same rectangular sketch is extracted for cavity
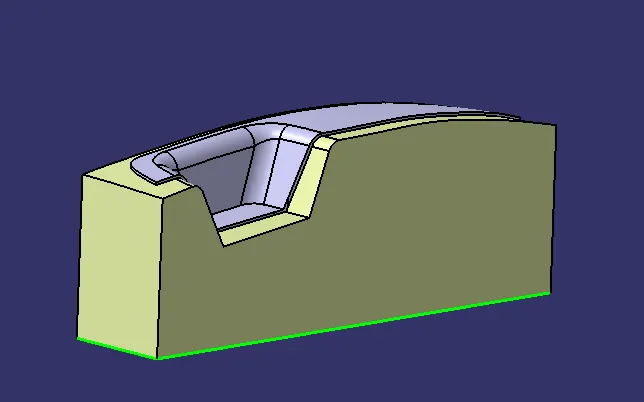
This is trimmed with B surface of switch bezel
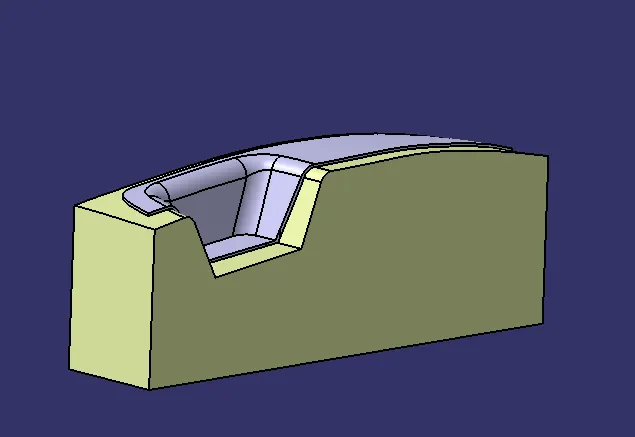
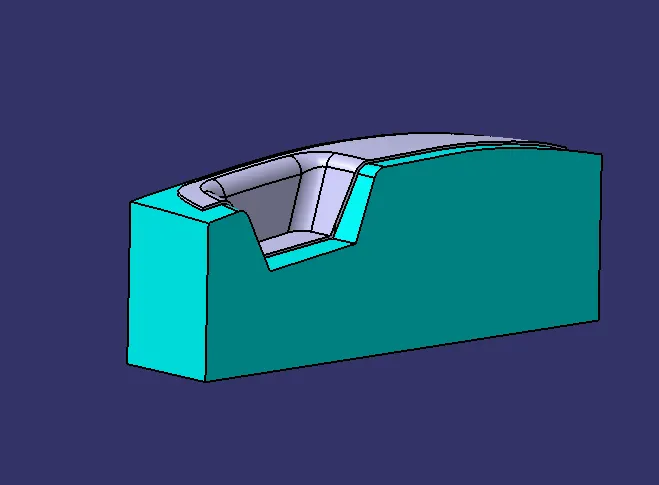
bottom is filled and joined to for cavity surface
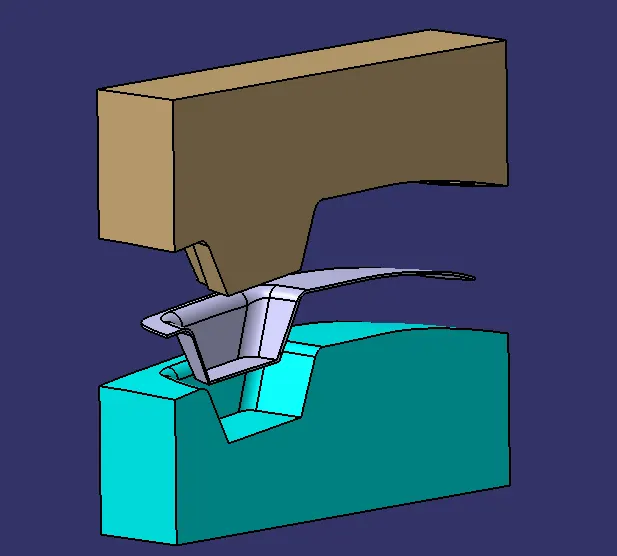
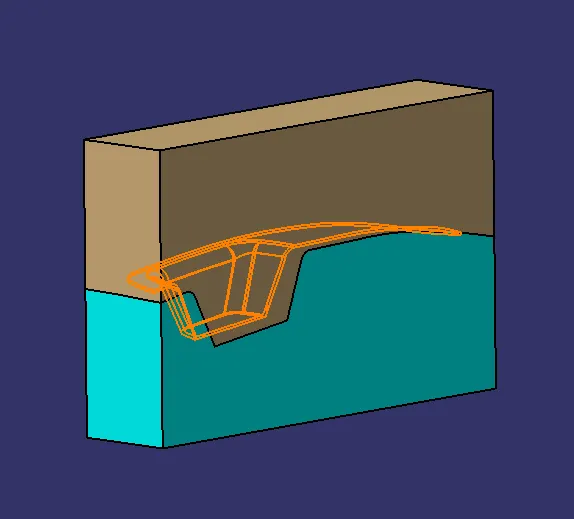
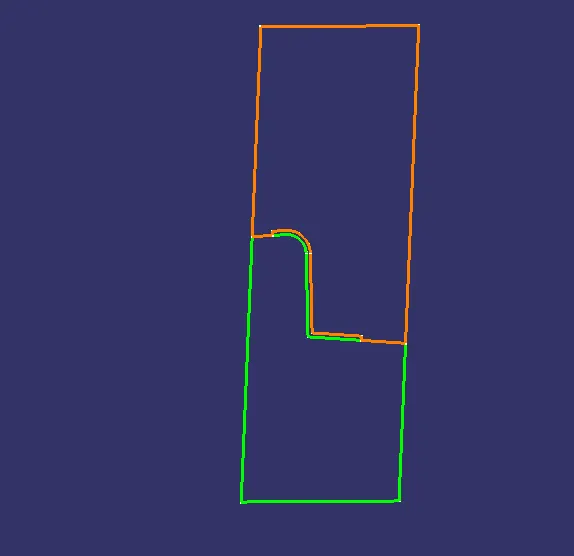
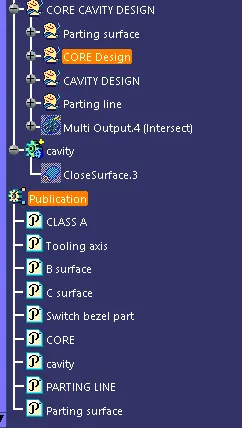
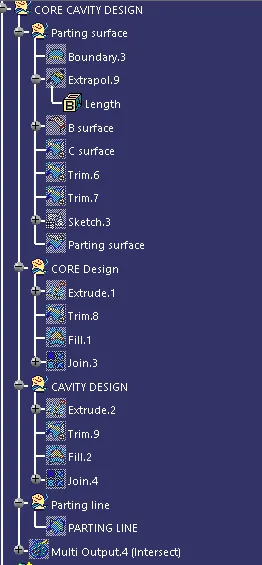
Geometrical set
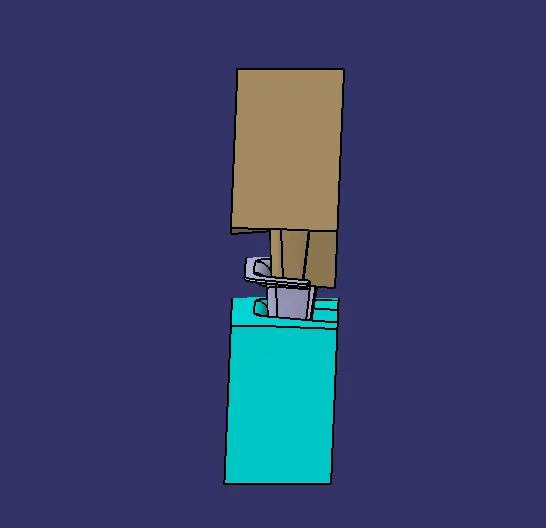
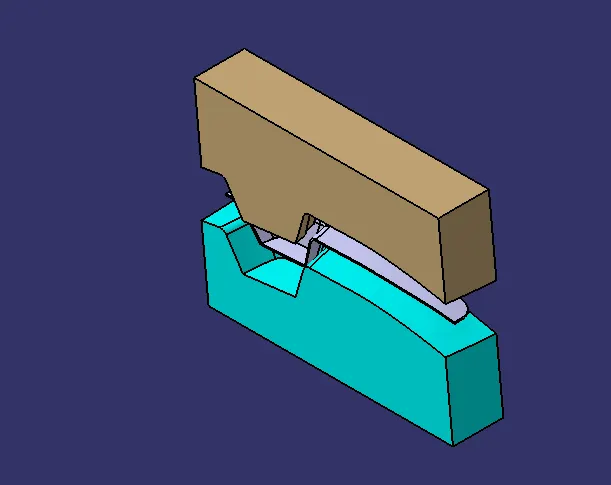
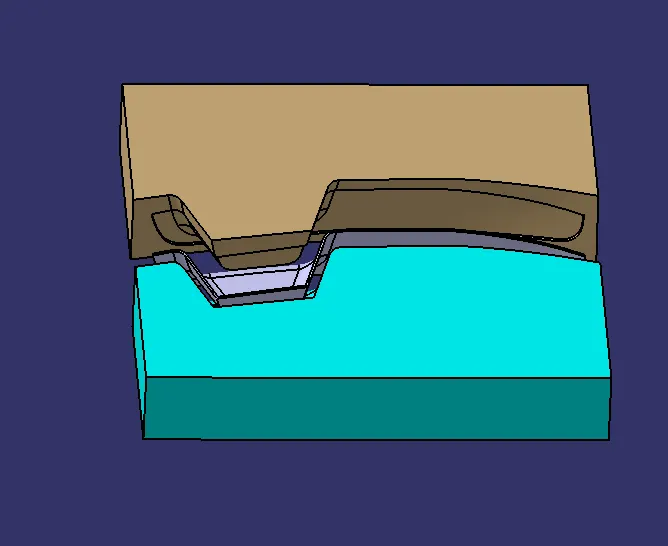
core and cavity blocks in various orientations