Week 1:- Introduction to BiW and Fixtures Challenge
- What is BiW & define its parts?
The stage in automotive design or automotive manufacturing in which the car body sheet metal components are been assembled by welding and by other joining process. Body-in-white (BiW) is the name given to a car body’s sheet when all its components—barring moving parts (e.g., hoods, fenders, etc.), trims (e.g., glass, seats, etc.), or chassis subassemblies—have been welded together. Usually, BiW constitutes about 27% of a car’s curb weight, and remains the key determinant of how the car will perform. BiW can be made into two structures: the more common monocoque structure where all body members are carrying load with chassis in-built with BiW and are integrated with each other, and the body-on-frame structure where the frame is the main load-carrying member
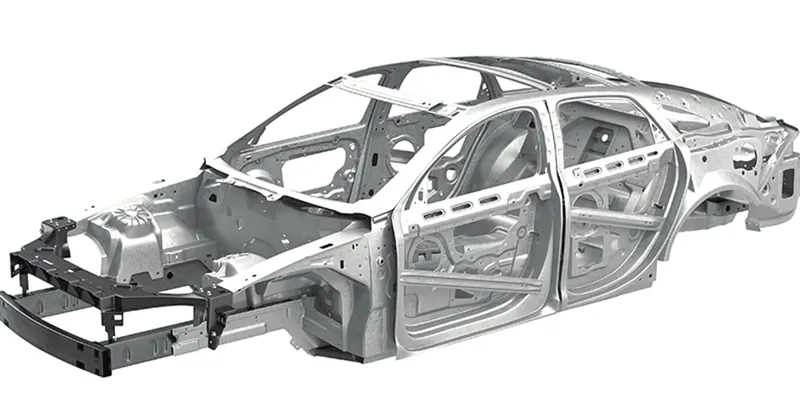
The BiW the parts are categorized as follows:
- Body sides-
- Outer body side
- Inner body side
- Under body
- Front end under frame (Engine compartment)
- Main floor
- Rear end under frame (rear compartment)
- Closures
- Front door
- Rear door
- Hood
- Deck lid
- Roof
- Roof inner
- Roof outer
- Fender
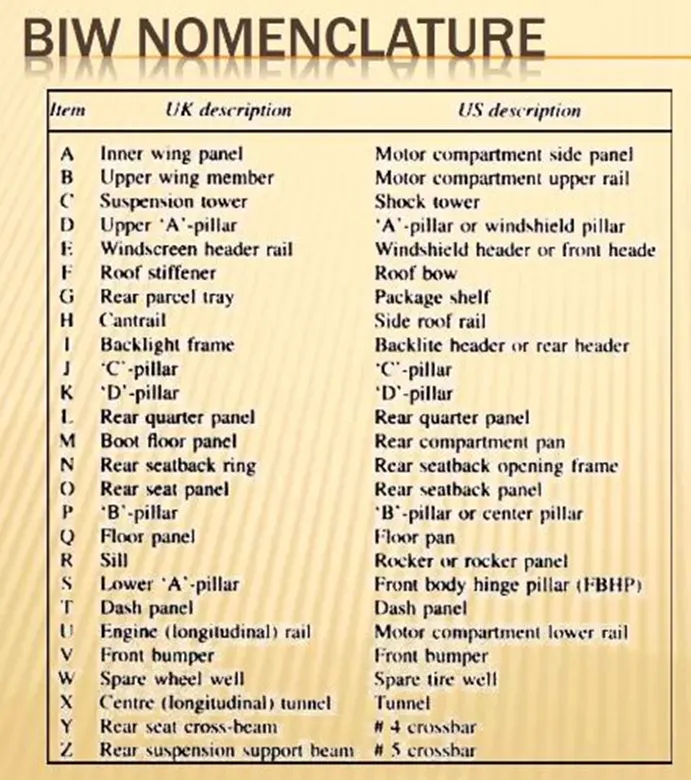
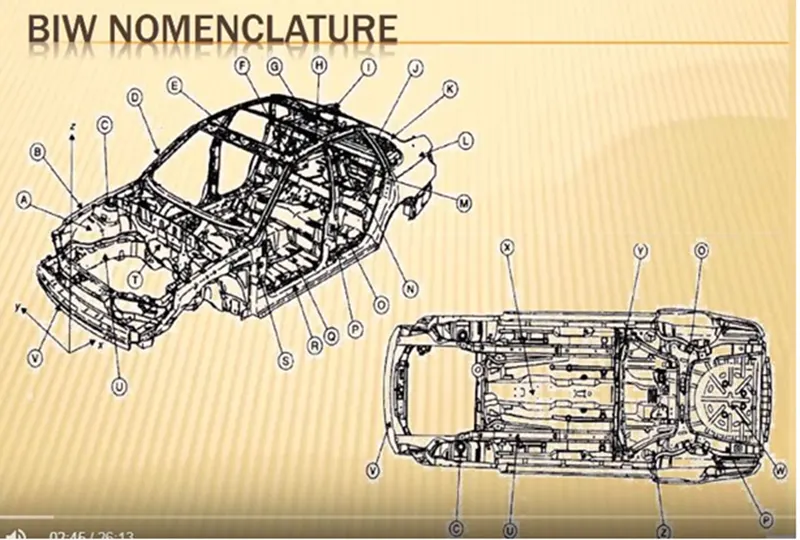
- What do you understand by BIW nomenclature?
BiW nomenclature is basically descried as the parts which are named for every individual parts with different standards, some of the standards are shown below
- What is fixture & its types?
Body in White (B.I.W.) refers to the welded sheet metal components which form the vehicles structure to which the other components will be married, i.e., engine, chassis, exterior and interior trim.
BiW fixture is basically a holding device which holds the parts to be processed, they are generally designed using the 3-2-1 principle. The main responsibility of the fixture is to hold the parts firmly and avoids the vibrations, distortion and any stresses induced, the processing area should be free from the fixture parts.
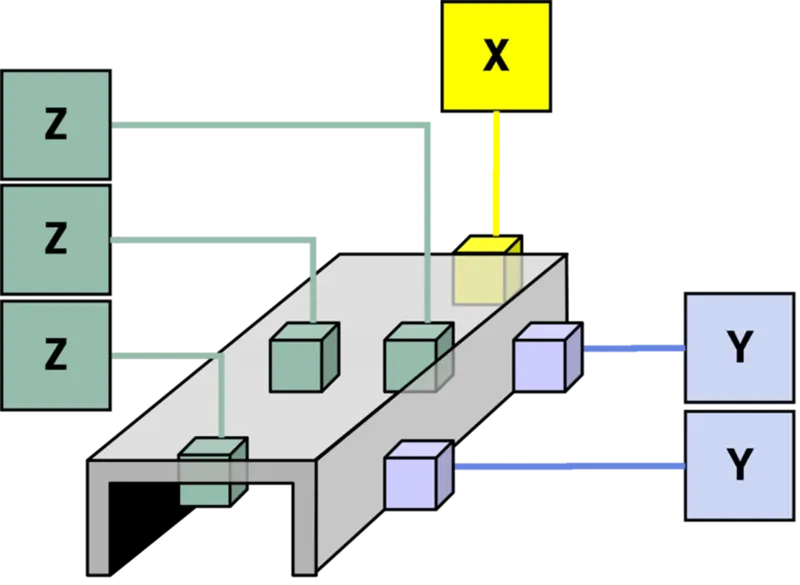
Basically 3-2-1 principle is used to lock all six degree of freedom.
The 3-2-1 principle is a Component holding principle, where three pins are located on the 1st principle plane, i.e., either XY, YZ, ZX. And two pins are located on the 2nd plane which is perpendicular to the 1st plane, and at last one pin on the plane which is mutually perpendicular to the 1st and 2nd planes. By using this method, Component can be arrested in all six degrees of freedom.
Types of fixtures:
- Production fixtures:
These are commonly used for mass production. Their features should be rigid, simple design and hard to withstand since it is used for mass production. These fixtures should be periodically maintained for efficient production. The loading and unloading at quick time period.
- Preproduction operation fixture
The fixtures are basically newly designed fixtures for the new products or parts. These may be complex, manual and heavy based on the application. These can be referred to as the prototype fixtures. Once the preproduction operation fixture functions properly, then modifications are made to improve and to make it simple and reliable.
- Checking fixtures
These fixtures are used for checking and inspection purpose. No processing is done in these fixtures. These fixtures consist of gauges for checking the dimensions and tolerances and its accuracies. In some checking fixtures, fixtures are fixed and CMM devices check the geometrical accuracies.
- What is the basic principle of fixture design?
Basically 3-2-1 principle is used to lock all six degree of freedom.
The 3-2-1 principle is a Component holding principle, where three pins are located on the 1st principle plane, i.e., either XY, YZ, ZX. And two pins are located on the 2nd plane which is perpendicular to the 1st plane, and at last one pin on the plane which is mutually perpendicular to the 1st and 2nd planes. By using this method, Component can be arrested in all six degrees of freedom.
- Elaborate types of BIW Stations?
- Geo station:
In this station geometry of two parts are fixed. it can be either using welding or riveting. In this station precision and geometry of the finished product is defined Locating pins have closer tolerance of 0/-0.15.
Suppose the hole dia of panel is 16mm then the pin dia minimum can be 15.85.
Diameter of locating pins should be lesser than the panel hole dia. So Tolerance in locating pin is given in negative value.
- Respot Station:
Once product comes out of the Geo Station and there are left out spots where spot welding or riveting is to be done. then it is moved to another station, that station is called Re-spot station.
These left out spots may be the due to clamp plan, cycle time, robot reach ability or any other various reasons.
In this station pins have tolerance up to 0/-0.28.
- Pedestal Station:
In this station, Pedestal gun is mounted on a tool and panel is manipulated manually or by robot to weld the panels.
Pedestal station is generally a Re spot station.
Re spot station and Pedestal station, both perform same kind of operation. but to decide whether to go for pedestal or a re-spot station some parameters needs to consider like cycle time, floor space, no. of welds, clamp plan, or size of the panel.
- Loading Station:
This station is used for loading of panel and same station is used to change the orientation of the if it is required in the upcoming station.
Sometime this station is used when Robots are unable to transfer panel from one station to another.
- Buffer Station:
This station is used to make the balance between the process.
Some stations carry out process in lesser time as compared to their respective stations. In that case panels can be stored in one station so that assembly line process remains smooth.
- Sealer Station:
In this station Sealant application is carried out. This process can be carried out manually or by using robots. Sealer is used in between two panels so that panels do not flatter due to friction.
- Marriage Station:
In this Station inner and outer panels are joined. In this station to avoid the impression on the outer panel (A class surface), copper strips are used in between the weld tip and A-class surface.
- Curing Station:
In this Station product received after sealing application, is kept idle at ambient temperature, which allows sealant to get dry with better bonding between the panel.
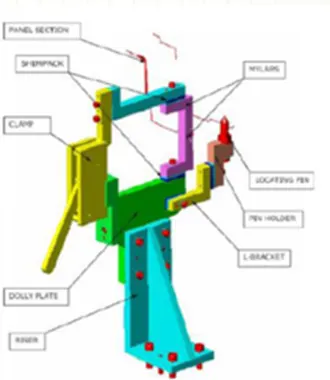
- What are the basic terminologies used in the BIW fixture?
The basic terminologies used in BIW fixture are:
- Principle locating point- These point help to accurately locate the part to maintain geometry of the assembly.
- Risers-These provide height and support to the assembly base
- Blade- These are plates mounted on the riser
- Shims- These are very small parts with lesser thickness, which helps to balance the dimensional tolerance.
- Rough locators- This is king of tool proofing which allows the operator to load the component only in the correct location and orientation.
- Hardware’s- These are bolt, nuts and self-locking nuts, etc.
- CMM- Coordinate measuring machine is the device that measures the geometry of the component using probe by physically sensing the discrete points.
- Unit: The fixture unit consists of different units some of them are base units, gripping units, etc.
- Number plate- It is a plate, which have numbers embossed on it. Which helps in recognizing the part later.
- Name plate- It is a plate which consists of the details of the fixture embossed on it.
- Clamp arm- It is an arm of the clamp which rotates along the pivoted axis
- Pivot- It is the axis or bearing about which the clamp arm rotates.
- Class-A or skin surfaces- These are the outer aesthetic components which are visible as the final assembly. While designing fixtures to such as parts the fixtures should be of soft materials and should hold firmly.
- Reed switches- These are the electric switches which are operated by the sensors or sometimes manually
- Sensors- These are the devices which are used to sense any part or component on the fixture and send signals to other mechanical or electric components.