Week 1:- Introduction to BiW and Fixtures Challenge
BIW (Body In White)
Body in White referred as Body in White is a structural shell of Sheet Metal Panels welded together to support subsystems in the vehicle. BIW holds a vital role in structural performance of the vehicle hence design with optimal materials is essential to reduce the overall mass of the component. BIW forms the base of the car body structure where the rest of the components are integrated to it and provides protection to passenger and cargo.
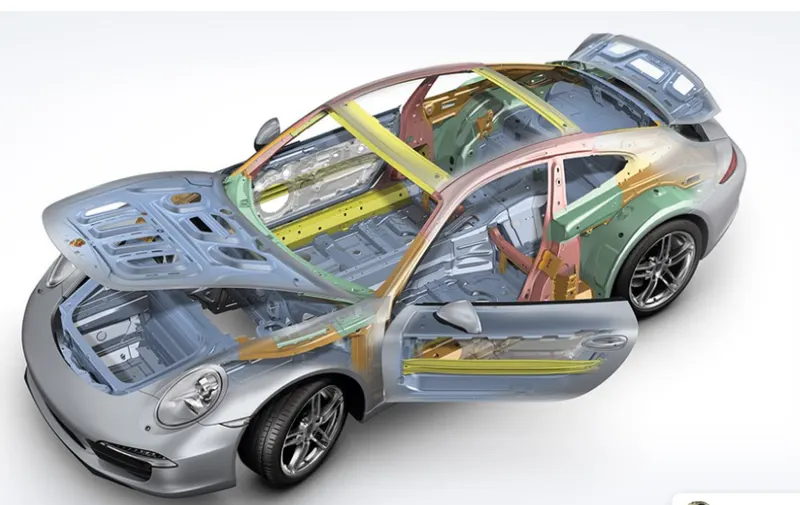
BIW Assembly line is divided in to two types; Upper body and under body. The parts involved in BIW structure are classified below
- Body Sides: Body side outer, body side inner
- Under Body: Front end under frame, Main floor, Rear end under frame
- Closures: Hood, Front door, Rear door, Tail Gate
- Roof: Roof Inner and Roof Outer
- Fender
Material Composition:
Significant properties of BIW are high tensile strength with high stiffness and bending including torsional rigidity. Hence the materials used are Steel, Aluminum and CFRP
|
Material |
Yield Strength (MPa) |
Ultimate Tensile Strength (MPa) |
|
Steel |
210–1250 |
340–1520 |
|
Aluminum |
90 |
195 |
|
CFRP |
250–585 |
The main aspects involved in BIW design are
- Aspects of aerodynamic design
- Design For Safety
- Styling & Branding
Thus BIW constitutes vital functions in Vehicle development involving various design considerations by adhering to safety regulations and guidelines.
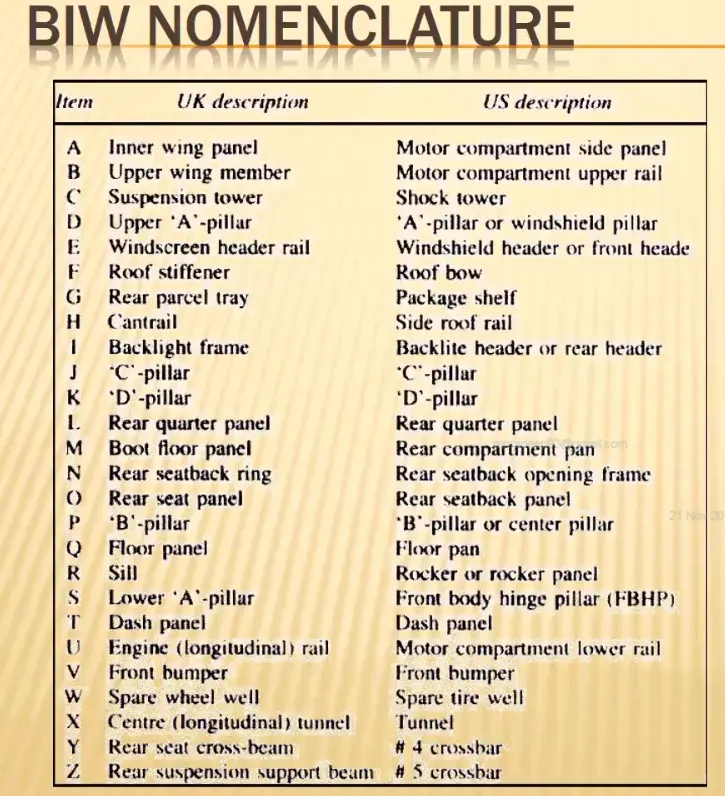
BIW NOMENCLATURE
BIW nomenclature is the process of tagging different names for the parts involved in BIW frame and therefore used for describing the parts and its properties.
An overview of parts used in BIW at two different region shows the emphasis of tagging names for the parts which are useful for collaborating vehicle for different geographical locations.
BIW FIXTURES
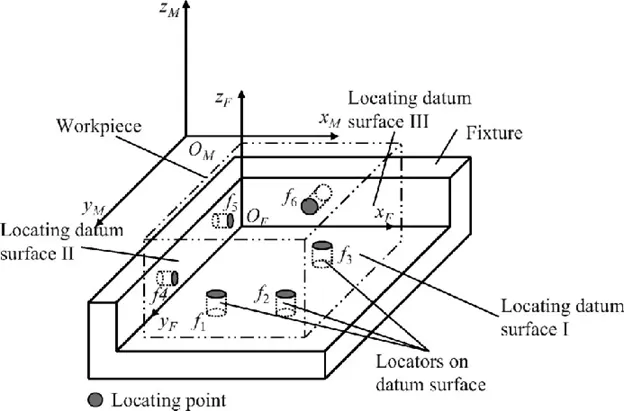
Fixtures are used for securing and locating various BIW Parts during different manufacturing processes. Each part requires special types of fixtures and respective operations and holds the parts in 3-2-1 principle.
Securing parts is absolutely necessary to avoid distortion in the work piece and clamping has to firm with correct location of parts. This enables a stable working environment and helps to withstand various stresses caused by different operations.
Fixtures are also useful during mass production which helps to achieve repeatability and automatic transmission between different stations by reducing variations in the parts produced during different operations.
The Types of BIW Fixtures are
- Production Fixtures
- Pre-Production Operation Fixtures
- Checking Fixtures
PRODUCTION FIXTURES
- They are used for mass production and are usually implemented after testing for dimensions, tolerances to reduce variations and are present in the shop floor till the final stage of production processes.
- The Productions fixtures are designed for feasible access to operators with affordable working space and easy to maintain.
- Automation levels are high in these types of fixtures as functioning of production fixtures are always tested before implementation.
Production Line BIW Welding Fixtures (Source: TATA MOTORS)
PREPRODUCTION OPERATION FIXTURES
- These are initial type of fixtures used for Pilot production to study and validate the process.
- Manual involvement is high as they are used for prototyping
CHECKING FIXTURES
- Checking fixtures are used for geometric inspection of car panels from the assembly.
- It is used to inspect the BIW panels post production to measure gaps and flushes, gauging accurate dimensions etc.
Checking Fixture for Underbody part
PRINCIPLE OF FIXTURE DESIGN:
The Principle of fixture design is defined as
- Rigidity
All bodies have 12 degrees of freedom; Six Translational and Six Rotational. It is essential to arrest these in order to locate the work piece in the fixture and thus the part is completely fixed avoiding any distortions or movements during operations.
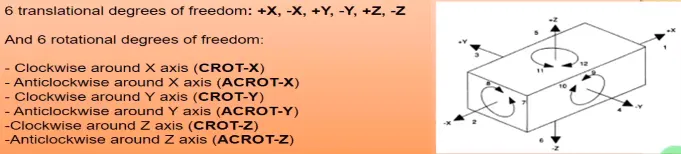
3-2-1 Fixture Scheme
- Fool Proofing
The Major part of fixture design is involved in how to locate the work piece in the fixture. The incorporation of design feature in the jig or fixture that will make impossible to lead the work in an improper position.
- Clearance
Apart from Fixture Design also involves providing ample space for working environment without interference and providing possible maintenance.
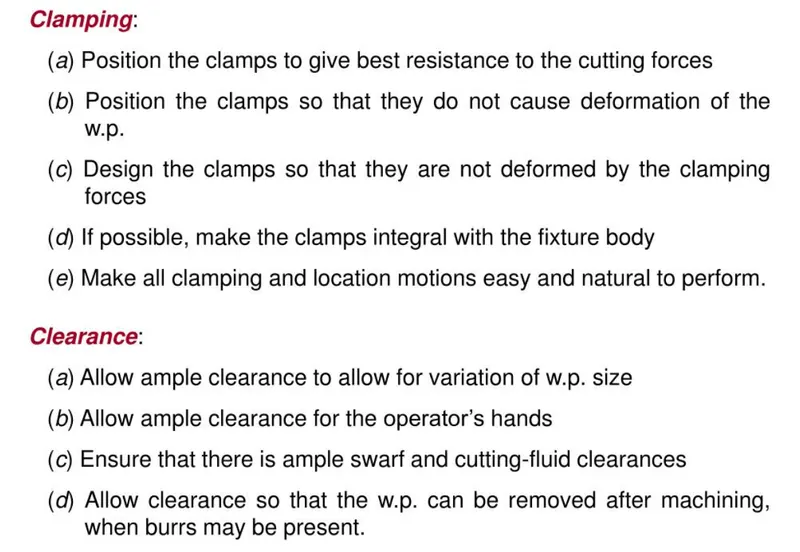
Thus these principles helps to achieve the function of fixtures thereby reducing the overall cost involved in producing the Automotive panel.
TYPES OF BIW STATIONS
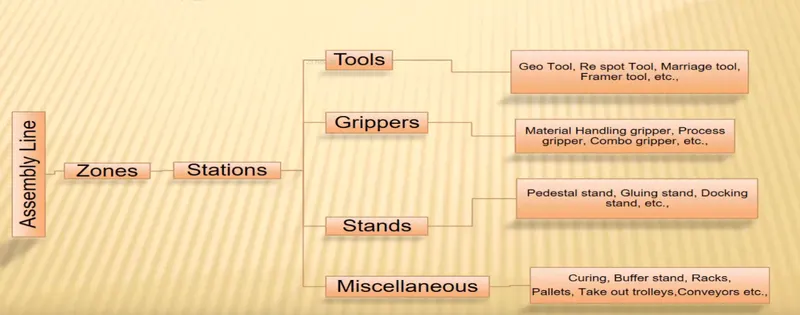
BIW Assembly line is where different types of panels are joined together in each specified zones. These individual zones are classified into stations such as tools, grippers, Stands and miscellaneous
TOOL STATION
Tool Station is where different parts are held together for manufactuing operation. Some of Fixtures used in tool station are
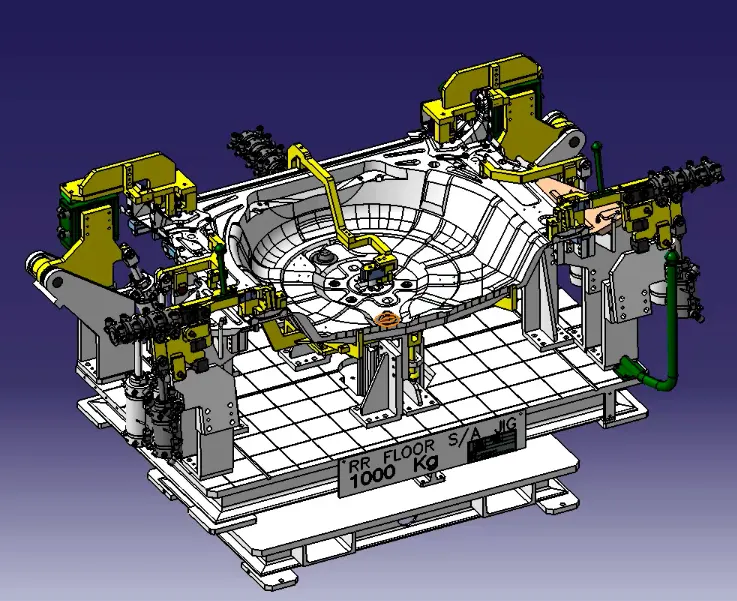
GEO TOOL:
- In Geo tool fixtures the geometry of the panel to be operated or held together very precisely with closer tolerances.
- For instance, a hole with dimension of 20 mm will have a pin designed with tolerance less than 0.15 mm.
- Thus Geo Fixtures help in achieving the geometry of the panels hence tighter tolerance are required to hold the panels firmly.
RESPOT TOOL:
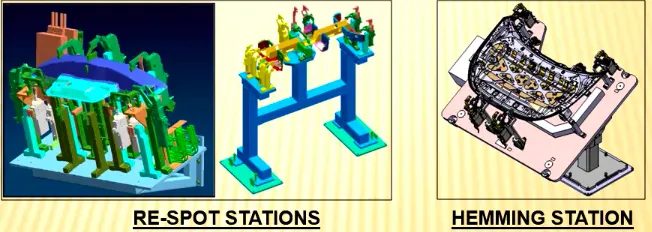
- In order to tackle the lead time and reduce the waiting time between two different station staions , not all welding spots are acchieved in geo fixture. Hence remaining tacks of prewelded panel are completed in Respot Fixtures.
- The tolerance standard for Respot Fixture is 0.28mm in general. Since Respot Fixtures are used for already welded panels there is a slight relacation in tolerance compared to geo fixtures.
MARRIAGE TOOL
- Marriage tool also called as hemming tool fixture is used to join inner and outer panels together.
- Hemming Fixtures are used to assemble specific components especially closure panels like Hood, Tail gate which has outer panel enveloped around the inner panel.
CHECKING STATION
- Checking station is used to gauge the processed automotive panels to ensure the coordinates, relative dimensions and position of parts as per tolerances
- The types of fixtures used in checking stations are gauge type, fixed type and automated checking fixtures.
GRIPPER STATION:
Gripper is type of fixture with lesser parts and weight compated Tool Fixtures and is used to hold the car panel.
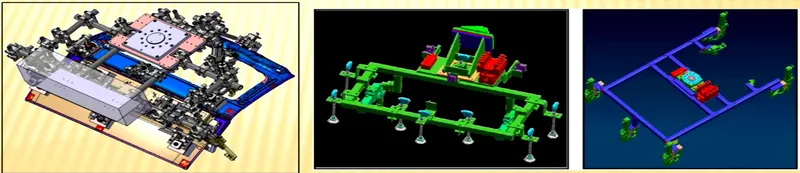
Type of grippers
The Grippers are attched to the manipulating end of the robots or End effectors. The types of gripper station are
Material Handling Gripper
Material handling gripper are used to transfer the part from one station to the other station.
Process Gripper
- Process Gripper are also used to transfer parts between station but in addition some of welding, riveting , gluing and sealing are performed intermediately between two process station.
- Thus after picking up part from one station the process gripper prepares for additional process by orienting the BIW panel for gluing, sealant etc before unloading in the next processing station.
COMBO GRIPPER
Combo gripper are used to transfer parts with additional weld gun or other processing station so it can multitask while transferring parts
DUAL GRIPPER
Dual Gripper have gripper on both sides which are used to transfer symmetric parts to be assembled between two stations.
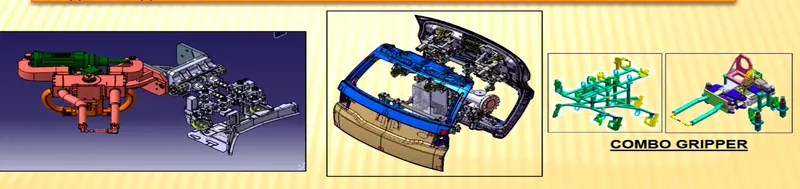
STANDS
Stands are used to bolster the operation of the fixtures and grippers and are attached to the floor.
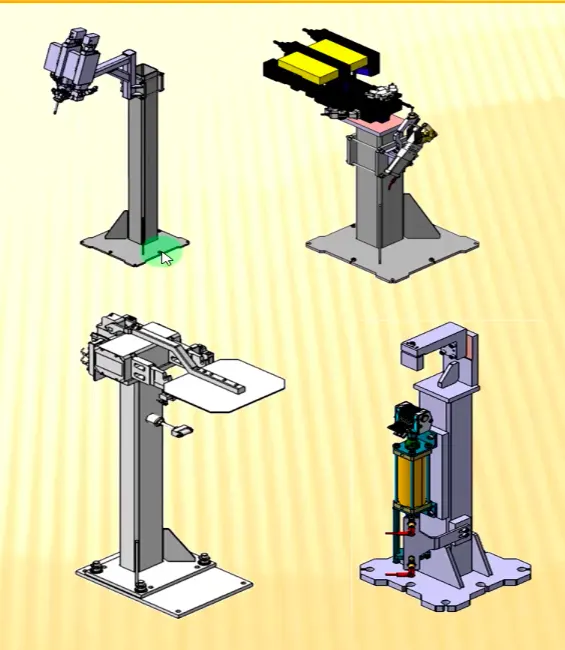
Gluing stand, Docking stand and Date stamp stand
They are used to resist vibrations while embossing or welding which might cause distortions
The types of stands are used are
Gluing and Sealer Stand
Gluing or welder gun is attached to the stand that are fixed permanently to the floor
Docking Stand
Docking Stand are used for placing welding gun or gripper while the fixtures are multitasking to avoid excessive payloads while material handling
Date Stamp Stand
The panel will get the date embossed on to it, with the date stamping device attached to the stand.
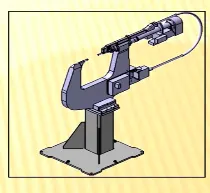
Pedestal Stand
Weld gun is mounted to the pedestal stand and pedestal stand are fixed to the ground. The processing grippers move the panels by passing below these pedestal stands.
MISCELLANEOUS STANDS
Buffer Stands: Buffer stands are used to hold the parts for while before loading in next station
Conveyer Stand: They are usually attached to conveyor belts and move from one station to the station
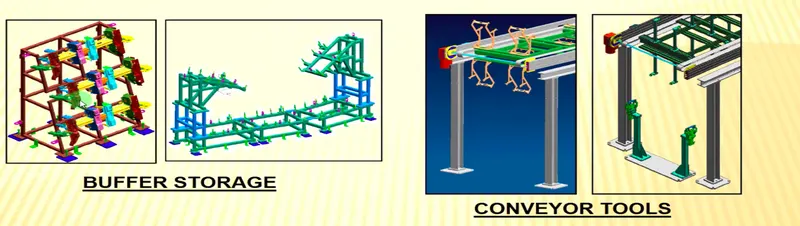
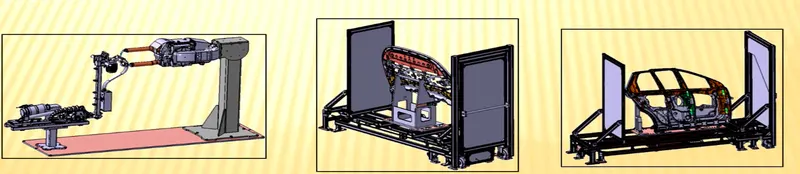
Take out trolley: Take out trolley is used to take the automotive panel out of the working station for inspection purposes.
Curing station: After welding and gluing the panels needed to cool for some time hence the assembly are allowed to cool with these type of stands
BIW FIXTURES: BASIC TERMINOLGIES
The basic terminologies used in BIW are,
1. NC/Mylars/Fingers.
2. PLP (Principle locating points).
3. Blade.
4. Raiser.
5. Shims
6. Rough Locators.
7. Hardwares.
8. CMM.
9. Units
10. Number plates.
11. Co - ordinate plates.
12. Name plate.
13. Clamp arm.
14. Pivot.
15. Class 'A' surface (or) Skin surface.
16. Reed switches.
17. Sensors.
MYLARS
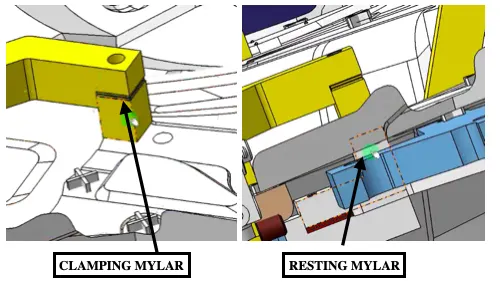
Mylars are clamping device used to hold on both side of the panel and usually have two parts clamping mylar and resting mylar.
PRINCIPLE LOCATING POINTS:
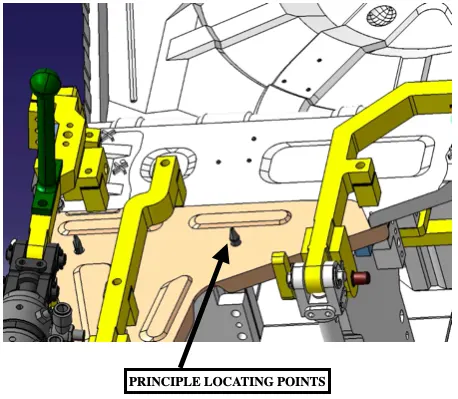
Principle location points (PLP) are used for accurate location of panel for maintaining the geometry of the assembly. The holes in panels are predefined in the design stages for accurate dimensioning so positioning of these holes relative to the dimensions are fealisble during fixture welding process.
RISERS
Risers are adjustable standing brackets that are used to define the height of the clamps and fixtures. Additional parts such as cylinders, mounting plate are also attahced to the risers.
SHIMS
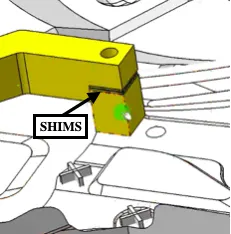
SHIMS are small thin tapered adjustments provided below the Mylars to negate the stack up analysis. In Worst Case Scenario the tolerance stack up and additional adjustments are provided through SHIMS to level the surface of the bed.
ROUGH LOCATORS:
In order to avoid the incorrect position of the panels rough locators are used for identification purposes for the operators
HARDWARES
Hardwares are general fastening devices like Nut, Screw, Bot, Washers etc.,
CMM
CMM is a Coordinate Measuring Machine. This device measures the geometry of the panel by gauging discrete points along the surface with a probe. This is used to inspection of the panels to validate with CAD file and generate reports for analysis.
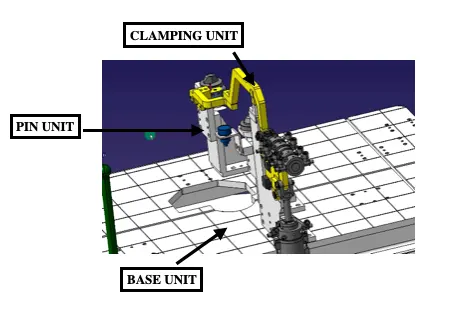
UNIT: There are different type of units that forms a fixture. They are classified as base unit, hole unit, pin unit, clamp unit
NUMBER PLATE: Number plate are embossed on the Fixtures for identification of various fixtures. Every Fixture poses a unique identification number that differentiates from other fixtures
NAME PLATE: Name plate holds the general description of the Fixture like Name, Weight, Company Logo etc.,
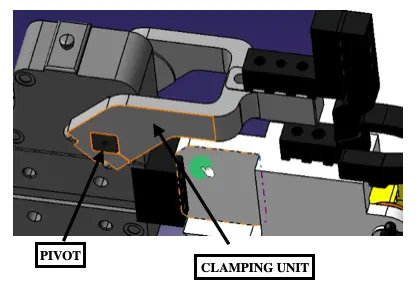
CLAMP ARM: In a clamp assembly unit the arm that moves are called as clamp arm
PIVOT: Pivot is the axis by which the Clamp arm will rotate in certain angle to either open the clamp and hold the clamp in close position.
CLASS A SURFACE: Class A surfaces are aesthetic Styling surfaces that are visible to the customers. It essential for Fixtures that are holding Class A surfaces are basked with soft material so that it will not leave any impression or dent on the CLASS A surface and it will not affect the surface texture.
REEDS SWITCHES & SENSORS
These are electrical units used for detection of panels and to automate the opening and closing of Clamp. Sensors are attached to the main panel and its subassemblies.
CONCLUSION:
Thus Automotive BIW and its Fixtures are elaborated with its basic nomenclature and terminologies.