Design of backdoor
AIM
Desing of BackDoor using given surface following proper parameter and design rules of sheeta metal . Also performe draft analysis on the part with accuracy.
INTRODUCTION
Back Door Of A Car:
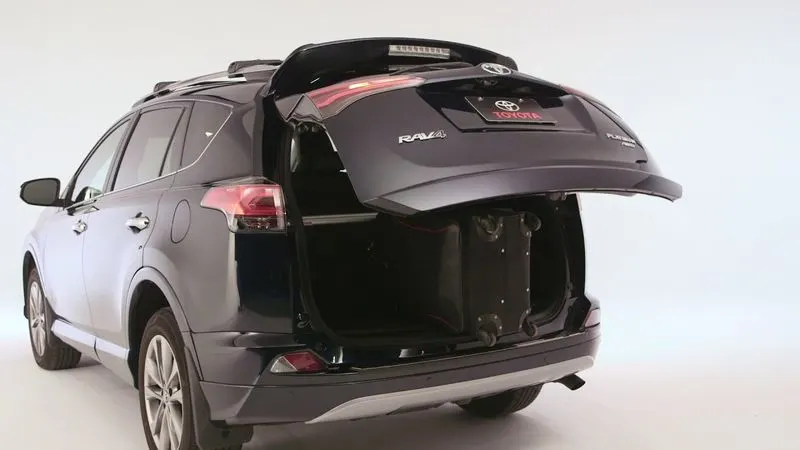
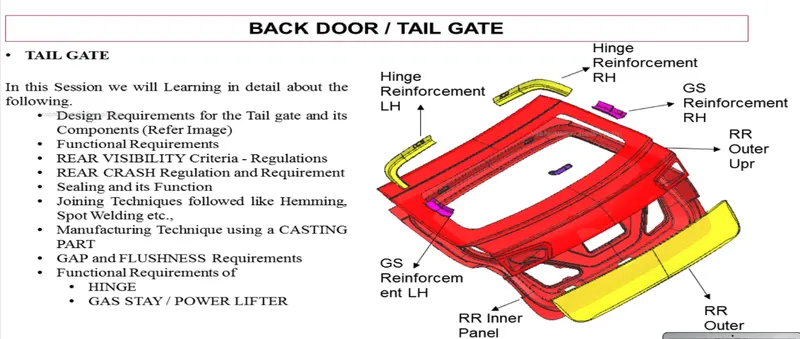
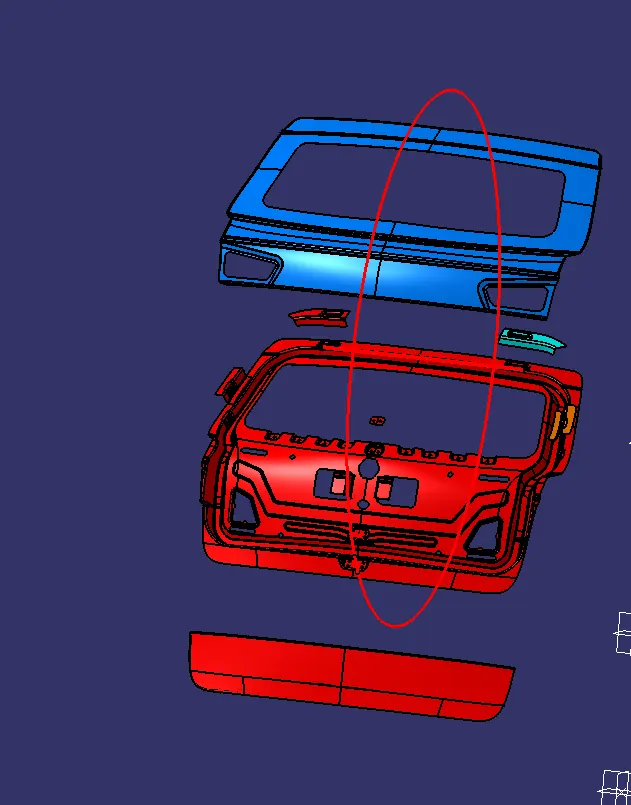
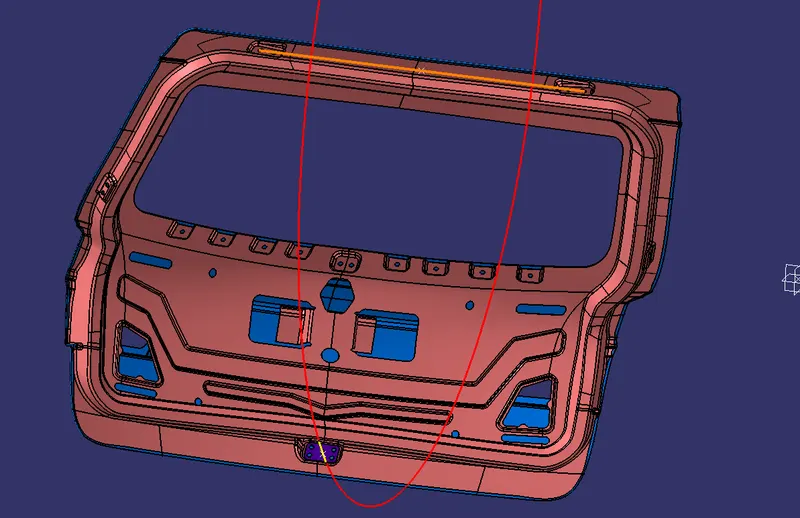
An automobile back door or Tailgate is the panel that covers the boot (or trunk) of an automobile. It enables access to the main luggage compartment. A hinge allows the boot lid to be raised, while devices such as springs or gas cylinders hold it up in the open position The Backdoor is an assembly of many parts such as inner panel, outer panel upper, outer panel lower and Reinforcement. Inner panel is attached to the outer panel using mastic sealant.
Back Door Variant:
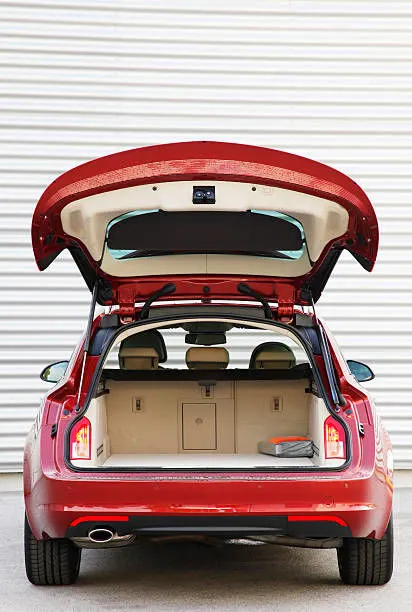
- Top Mounted Door
- Side mounted Door
- Bottom Door
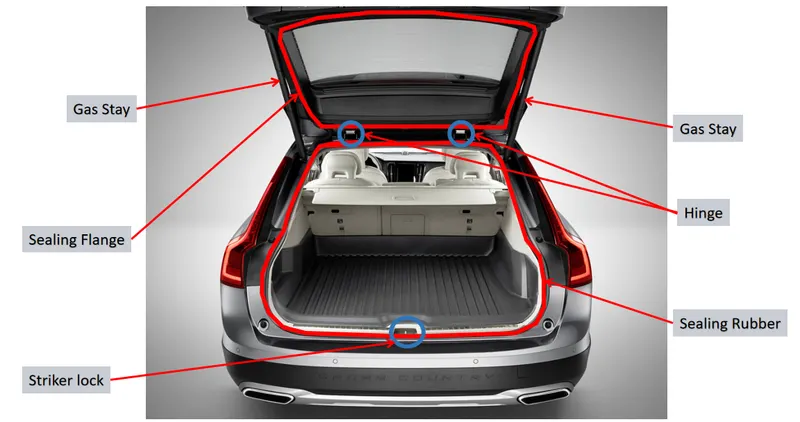
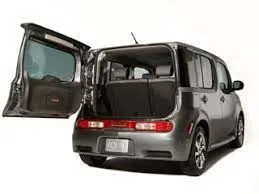
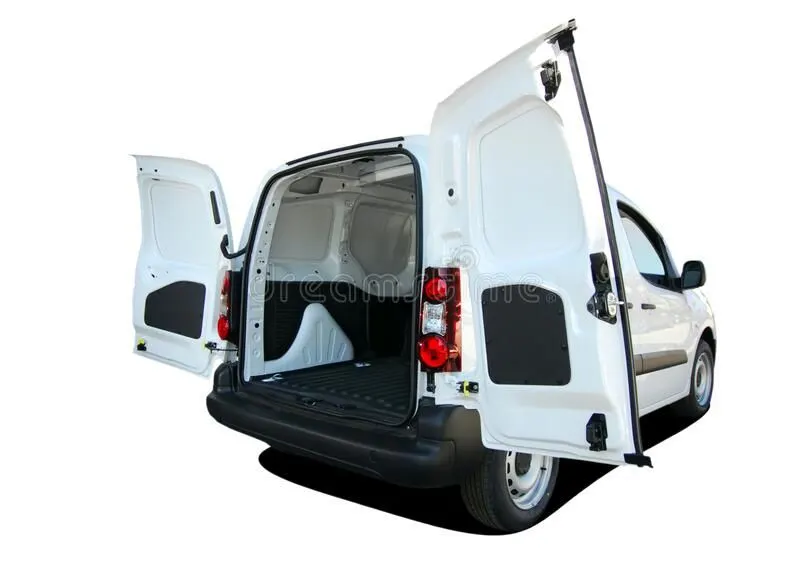
Gas Stay Powered:
Hands Free Power Back Door:
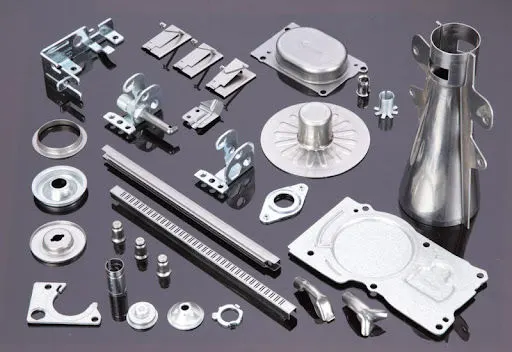
PROCESS SHEET METAL MAFACTURING
1- Deep Drawing:
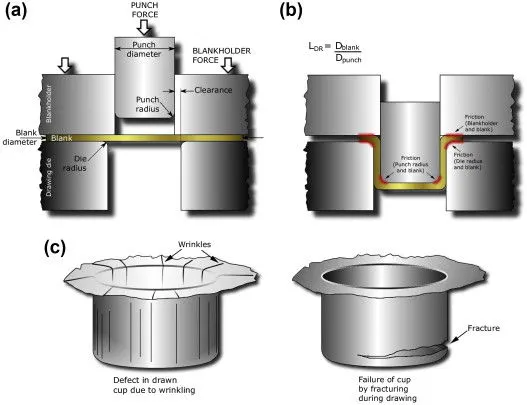
- The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions. A flat sheet metal blank is formed into a hollow body open on one side or a hollow body is formed into a hollow body with a smaller cross-section.
- The process results in scratch-free parts regardless of the sheet thickness or complexity of the tool, including undercuts. High forming pressure ensures close tolerance parts direct from the press with little or no secondary hand work required.
- The process is considered deep when the depth of the drawn part exceeds its diameter. This is achieved by redrawing the part through a series of dies.
- These compressive stresses, hoop stresses, result in flange wrinkles. These wrinkles can be prevented by using a blank holder, the function of which is to facilitate controlled material flow into the die radius.
- The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
2-Embossing:
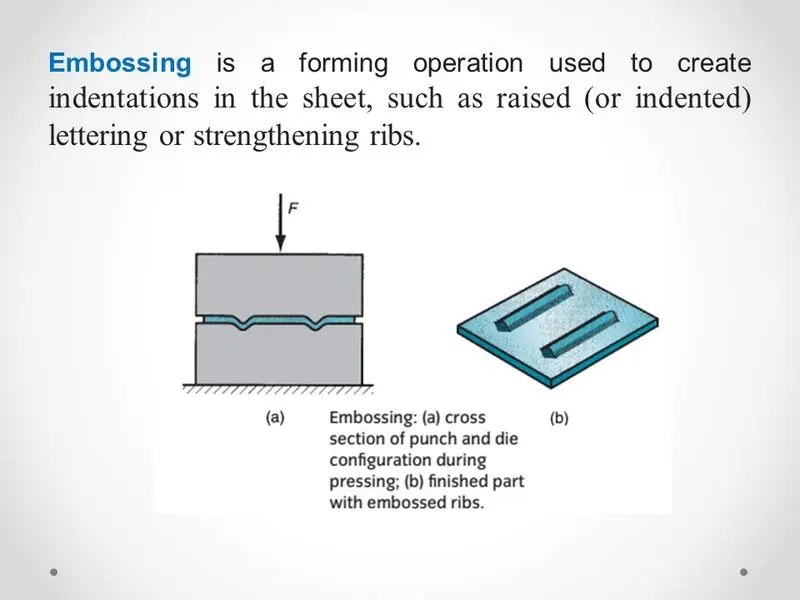
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
3-Hemming:
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
There are various types of hemming operations:
- Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
- Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
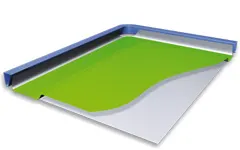
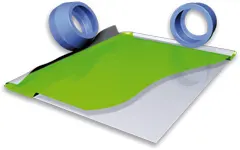
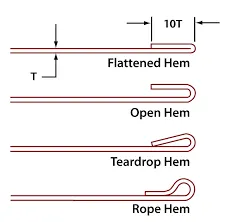
Open Hem: A Hem has a full round feature and a return flange. In open hem bend angle is equal to 180 degrees.
Tear drop Hem: In tear drop hem the bend angle is greater than 180 degrees.
Closed Hem: Hems without any inside radius are called as closed hem. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
4-Blanking:
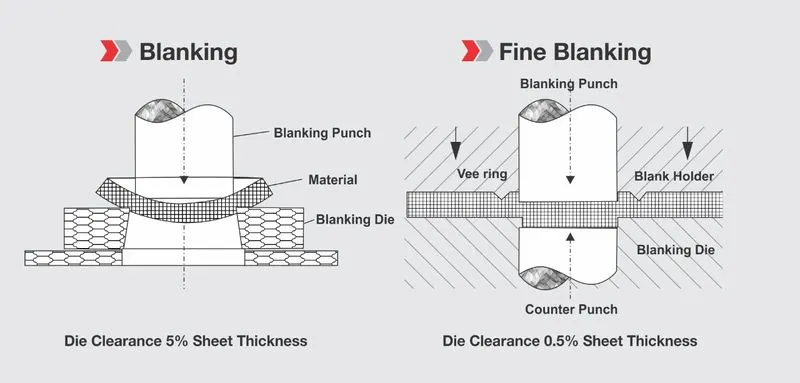
Blanking is a metal production process, during which a metal workpiece is removed from the primary metal strip or sheet when it is punched. The material that is removed is the new metal workpiece or blank.
5-Punching
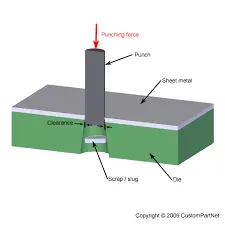
- Sheet metal punching is a cutting process in which material is removed from a piece of sheet metal by applying a great enough shearing force.
- CNC Punching can be used to produce holes and cutouts of various shapes and sizes.
- The most common punched holes are simple geometric shapes (circle, square, rectangle, etc.) or combinations thereof.
- The die, located underneath the sheet, has a cutout in the shape of the desired feature.
- Punches and dies of standard shapes are typically used, but custom tooling can be made for punching complex shapes.
- The punch press drives the punch downward at high speed through the sheet and into the die below.
- There is a small clearance between the edge of the punch and the die, causing the material to quickly bend and fracture.
DESIGN CONSIDERATION
The following are the Design considerations taken while designing the Back Door. They are,
- Visibility Criteria
- Force Dissipation
- Latch and Stricker Positions
- Hinge Position
- Gas Stay Position
- Material Selection
- Space Availability
- Hemming and Relief Areas
All these design considerations go hand in hand with eachother because these positions are dependant on each other and if position gets altered all the positions has to be altered for effective opening and closing of the back door. The Latch and Stricker, Hinge Position and the Gas stay Positions has to be maintained in a proper way so that they play a major role in the opening and closing as well as the rear Visibility criteria of the car.
Material Selection:
The material selection play a major role in determing the overall weight of the back door. The materials generally used are Steel and Aluminium. The Density of Steel is higher than Aluminium thus it results in adding more weight of the door. Basically the material is used based on the budget of the car, because the cost of steel very cheap than Aluminium. If aluminium is used instead of steel there is no need of many parts like Reinforcements for each mounting and the overall weight geta reduced by 6-10 kg approximately. But the draw back is Aluminium is much costlier than Steel. Hence based on the budget of the car aluminium is used. In higher end models like Benz, Audi, Porshe and BMW we can find aluminium is used instead of steel resulting in reduced weight and increased performance of the vehicle.
Another Factor to make a note is using Casted Aluminium instead of deep drawn Steel components and adding reinforcements to it is the space of the luggage commodity gets increased by a certain amount because the draft angle for Casted aluminium is much lesser (3 degree) than the deep drawn Steel inner panel (7-9 degree). Thus it reduces the space between the inner and outer panel resulting in much larger cabin space than the deep drawn steel inner panel. Thus the material selection is one of the design consideration taken. Since it reduces the space between the inner and the outer panel the rear visibility of the car is also inproved giving more space for the mirror to view.
Hence in this design the material chosen is steel since it is designed for a medium budget car and hence high cost could not be afforded to design the back door.
Force Dissipation:
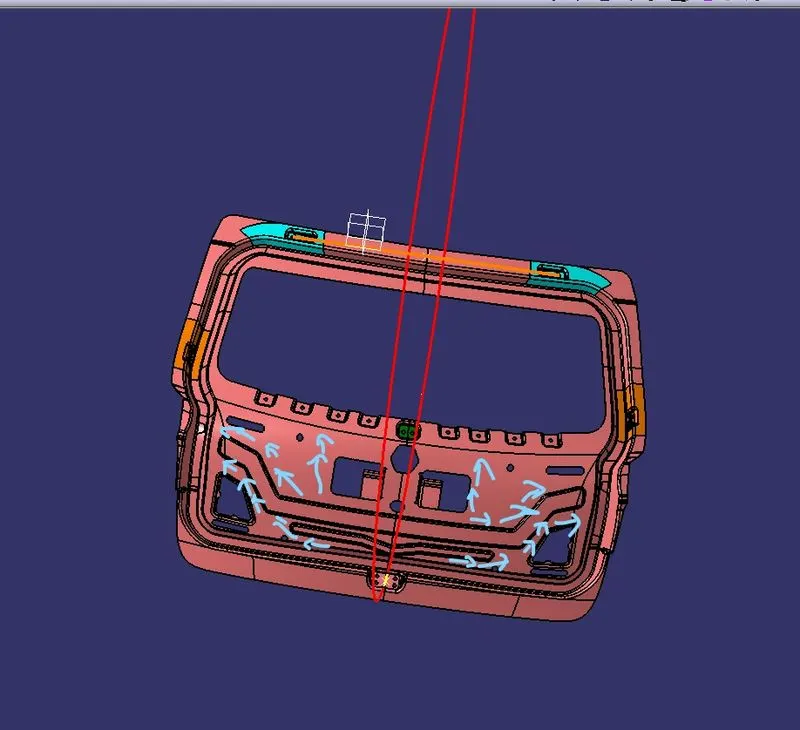
The major criteria in designing the back door or any BIW part is the force dissipation during an impact or a colloision. Hence studies are being done inorder to dissipate the force on the sides and avoiding it reach the inner cabin of the car so that possible damage of imapct inside the car is reduced. Hence inorder to do that the V or Y embosses are created on the inner panel so that the force gets transmitted on to the sides instead reaching it on the cabin. This is one of the main criterias in back door design.
Latch and Stricker Positions:
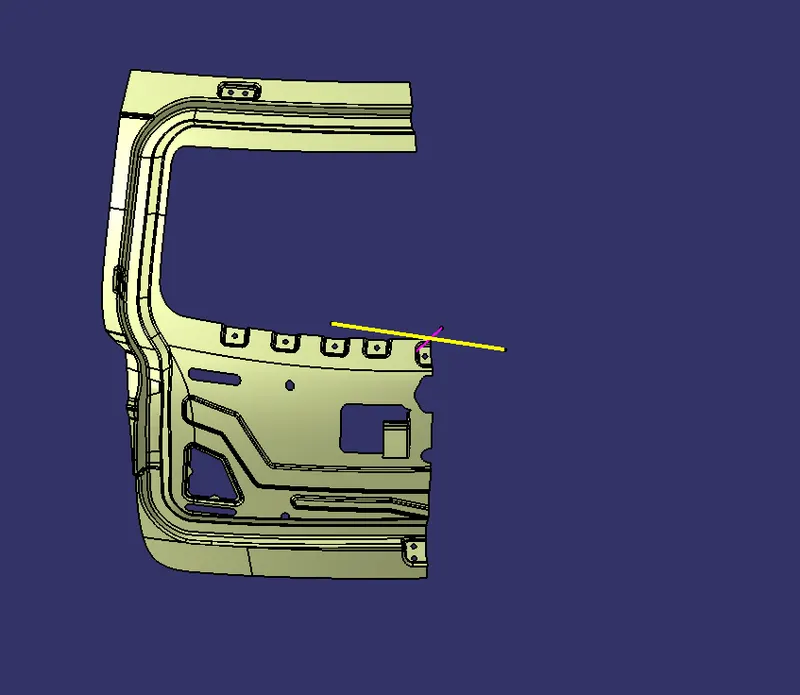
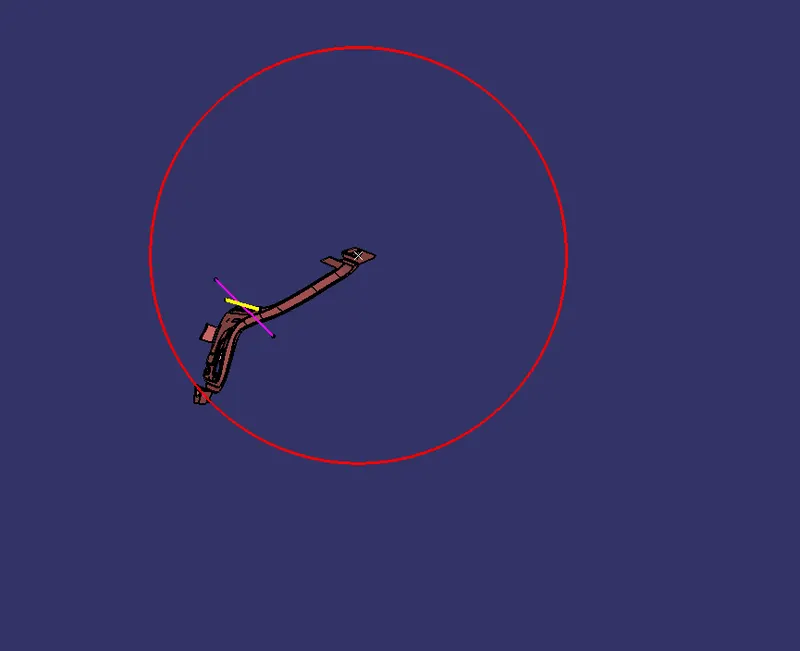
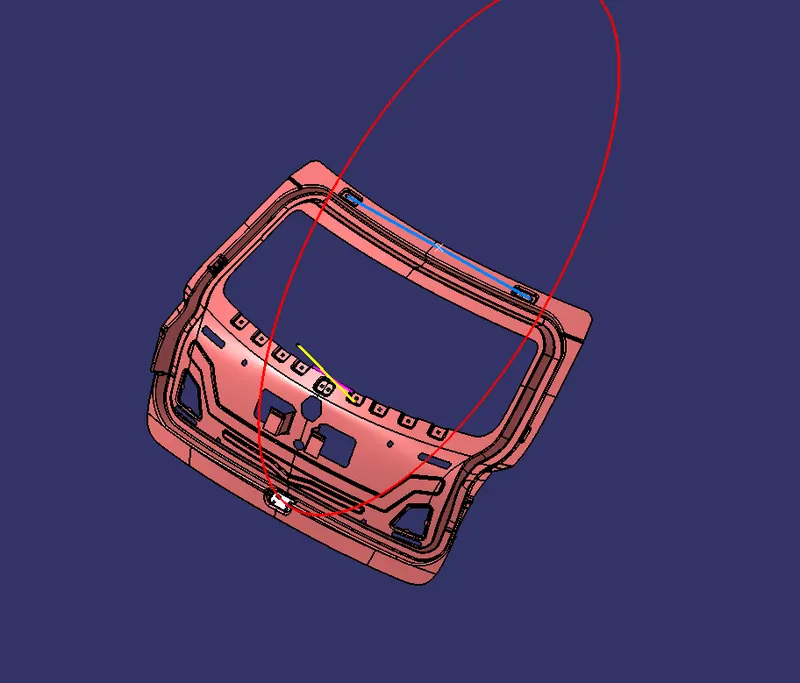
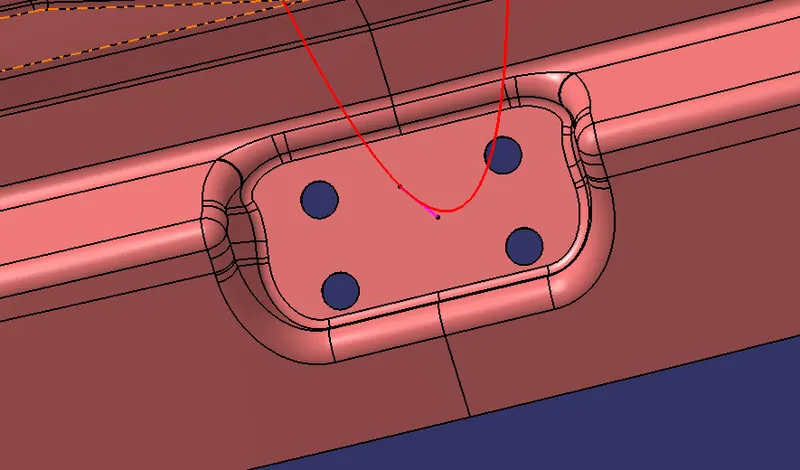
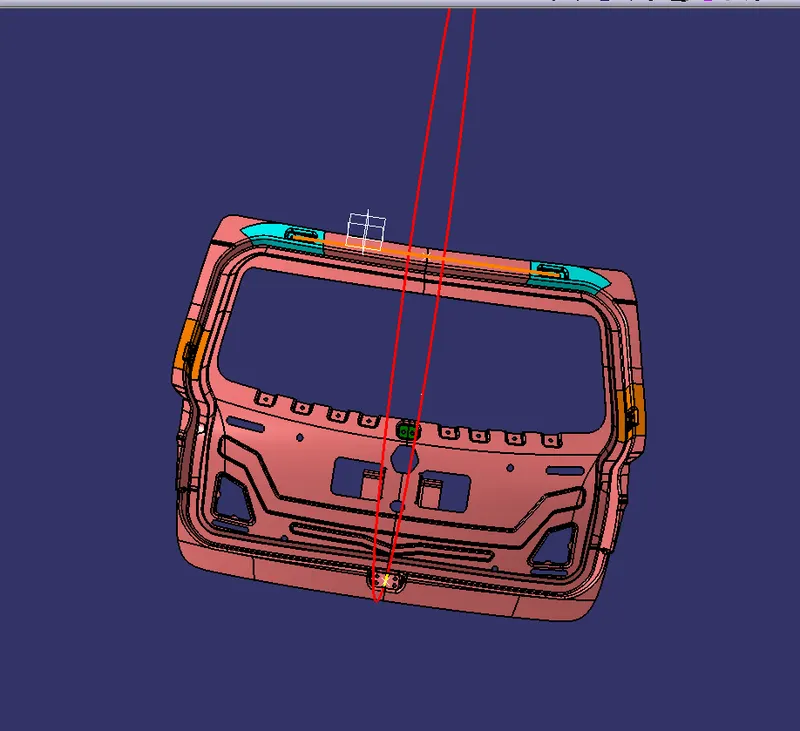
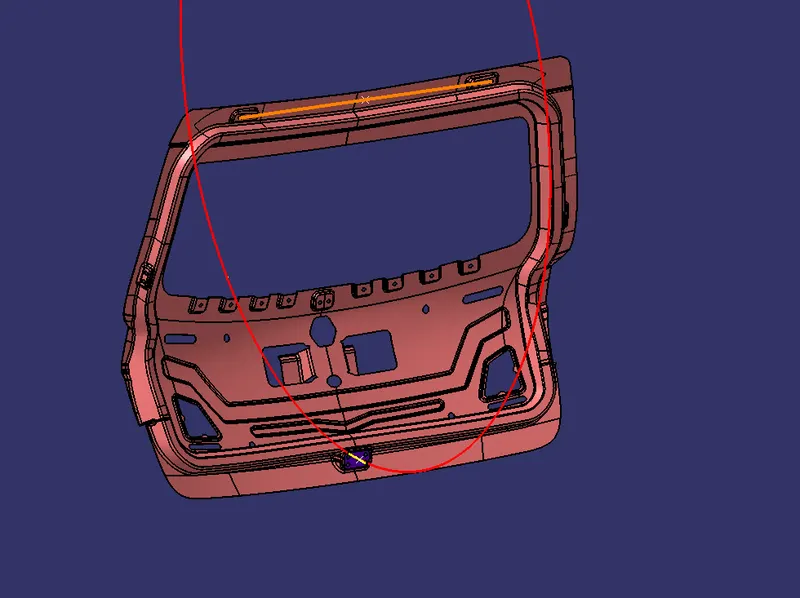
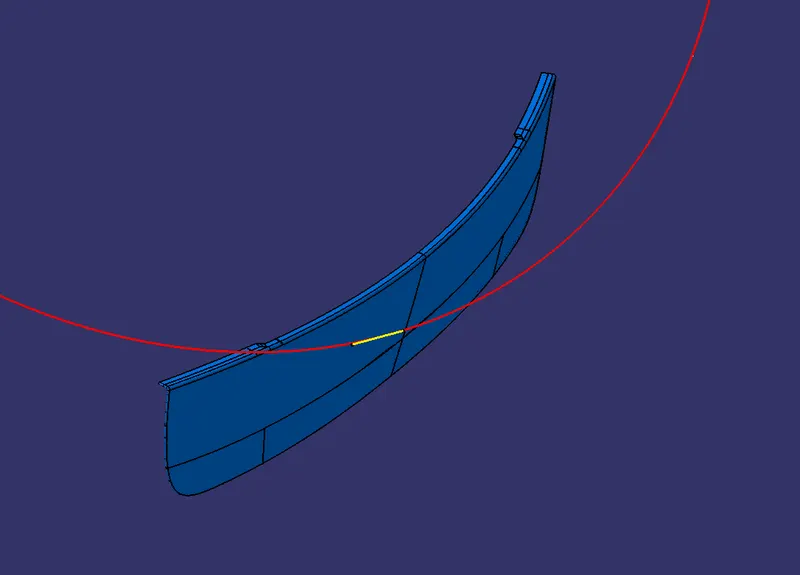
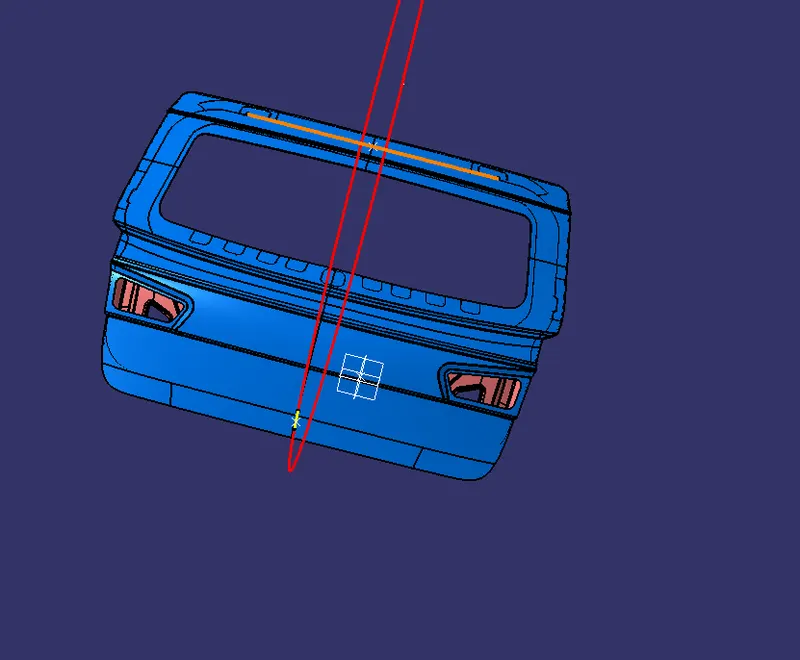
The Latch and Stricker positions play a major role in determing the opening and closing of the back door. Hence the opening and closing of the had to smooth and inorder to ensure that the the centre point of the latch and stricker has to to be at the same point and the trajectory has to be tangent to the open close circle that is drawn. This is shown in the below image. Only if the centre points and the tangent line are perfect the opening and closing of the back door is smooth and clear. Or else the Hinge positions, Gas stay positions and Latch and Stricker Positions has to be altered to meet the change.
Hemming and Relief Areas:
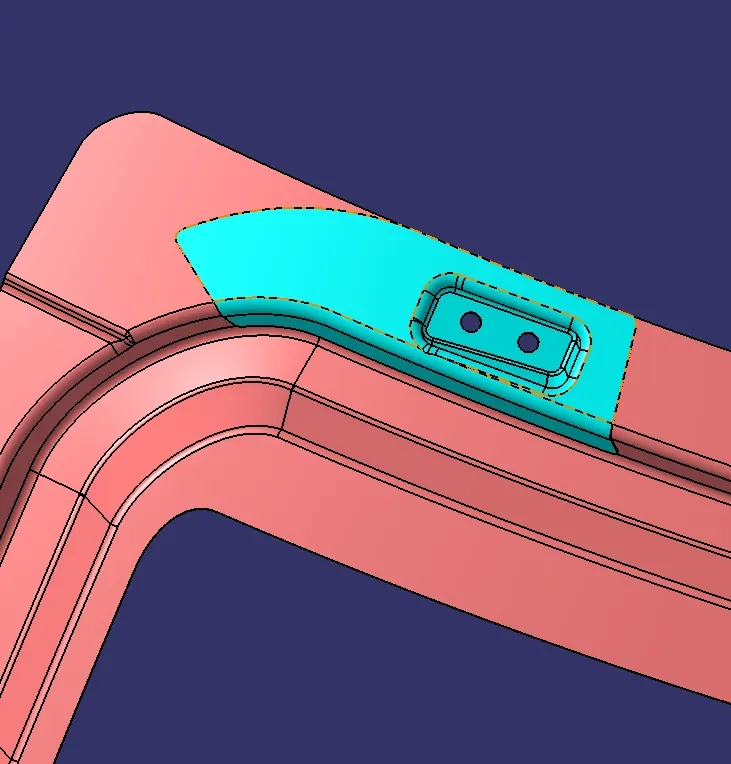
Hemming and Seaming are two similar metal working processes in which sheetmetal edge is rolled onto itself.Hemming is the process in which the edge is rolled flush to itself, while a seam joins the edge of two materials.
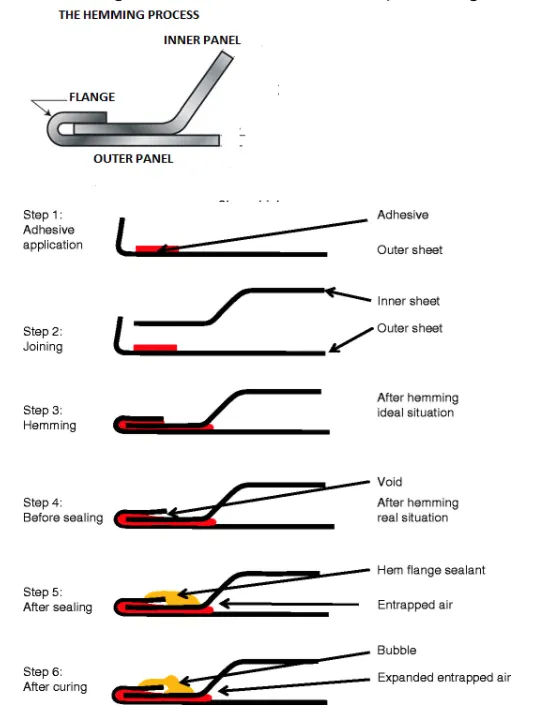
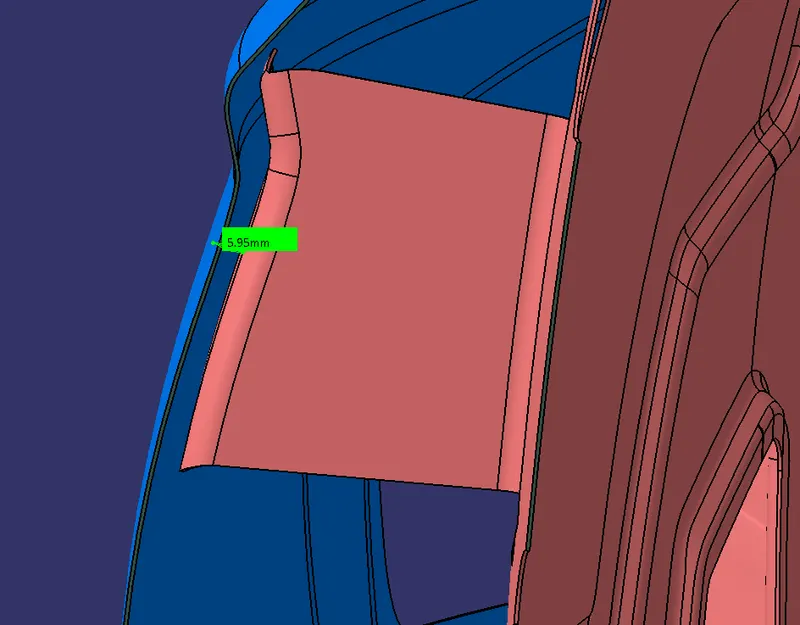
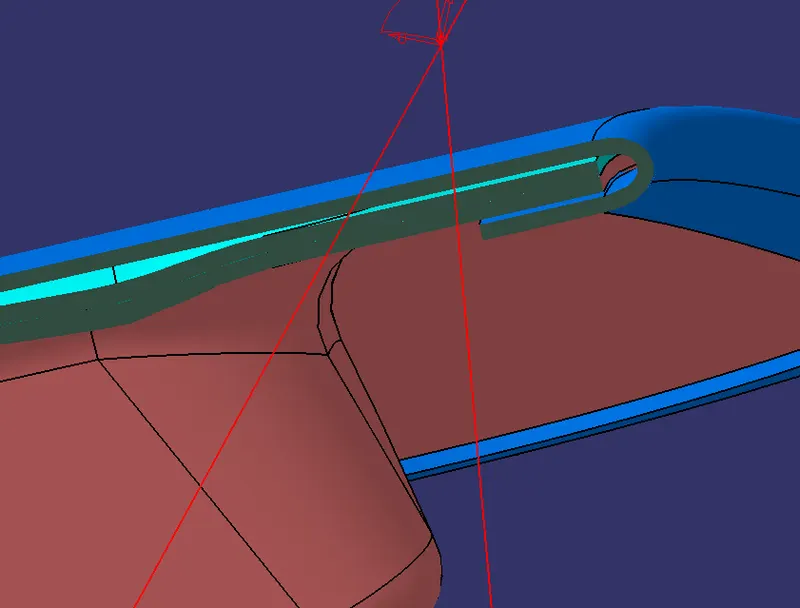
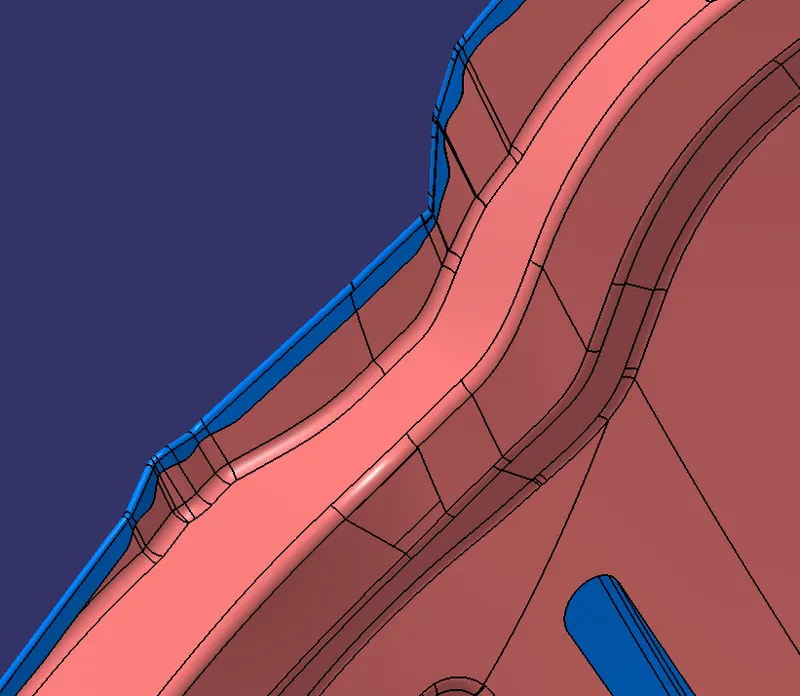
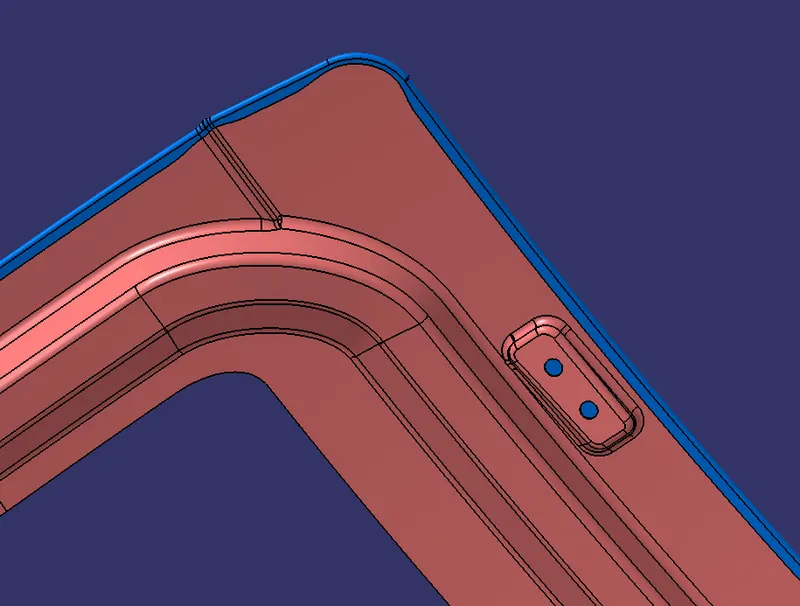
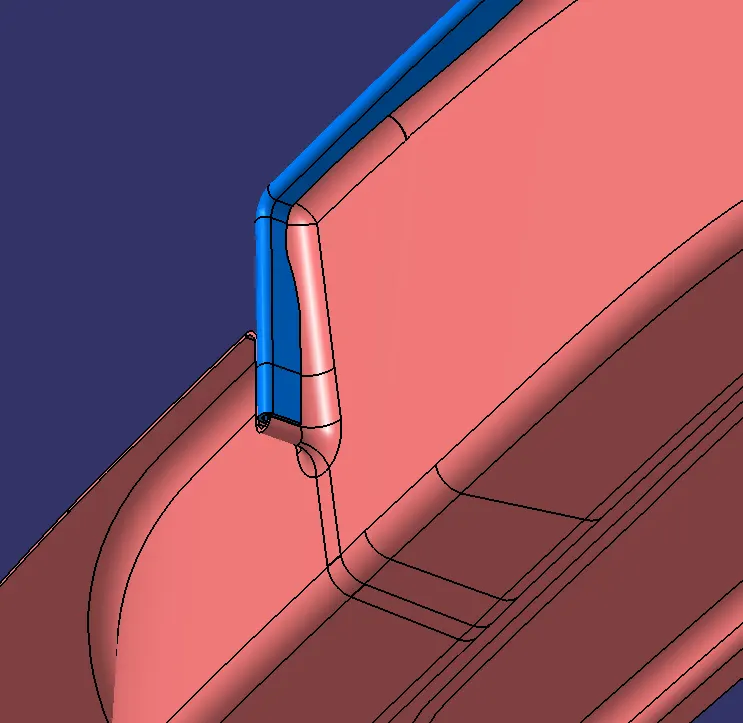
The Hemming is done on the outer and the inner panel with an clearance of 0.2mm on the either sides. Since at the corners the hemming is difficult to perform, clerances has been given at the ends of panels so that it would for the hemming operstion is performed. Here is the image of the hemming relief at the corners.
DESIGN OF BACK DOOR
-Back Door Assembly Consist Of :
- Outer Panel
- Inner Panel
- Hinge
- Latch And Striker
- Gas Stay
- Wiper Motor
- Reinforcements
Procedure:
Step-1
- Door parts thickness are to be followed
- Outer Panel - 0.75 mm
- Inner Panel - 0.75 mm
- Reinforcements - 1.5 mm
- Then Analaysis of the given styling surface.
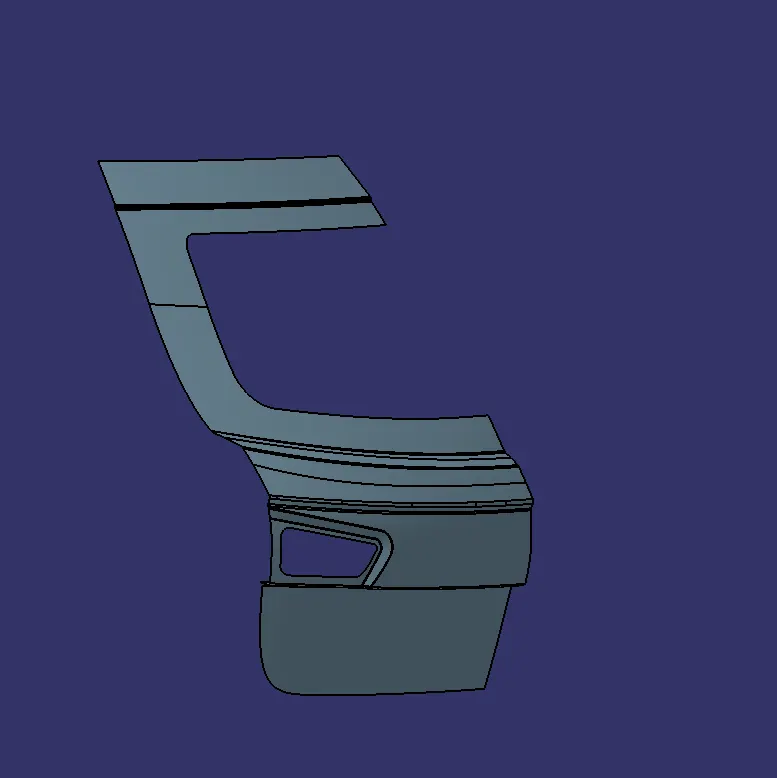
Step-2
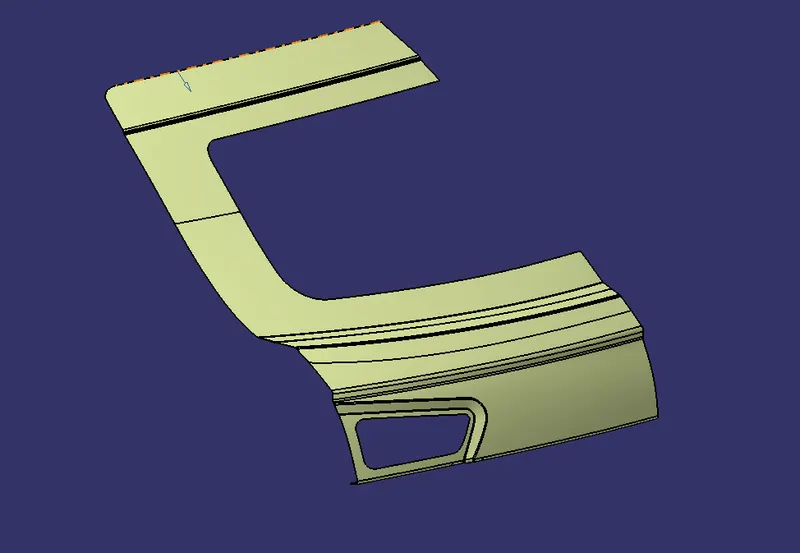
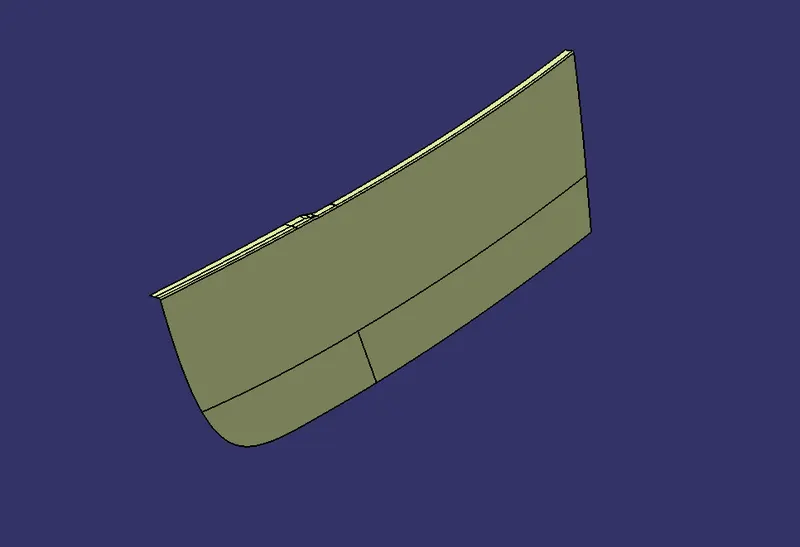
- Work on given surface for removal of anomalies present on the surface to make it flow smoothly.
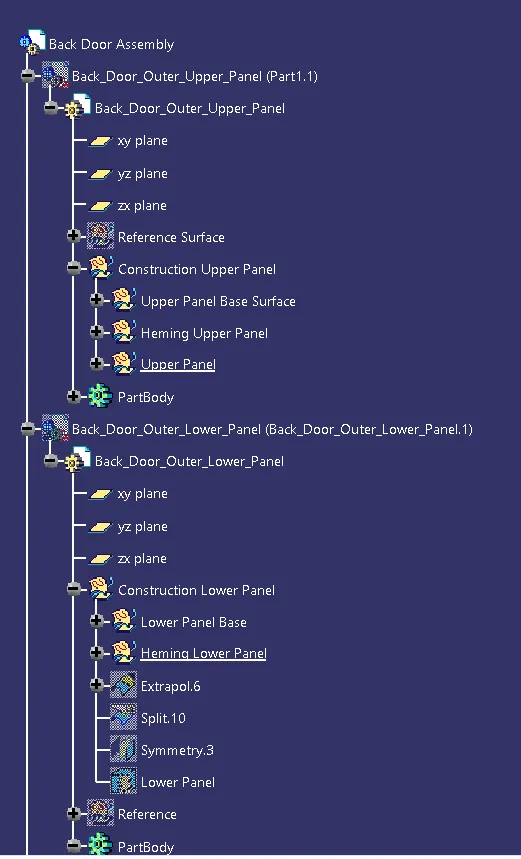
- Also separate Outer upper and lower into two different parts in assembly.
Step-3
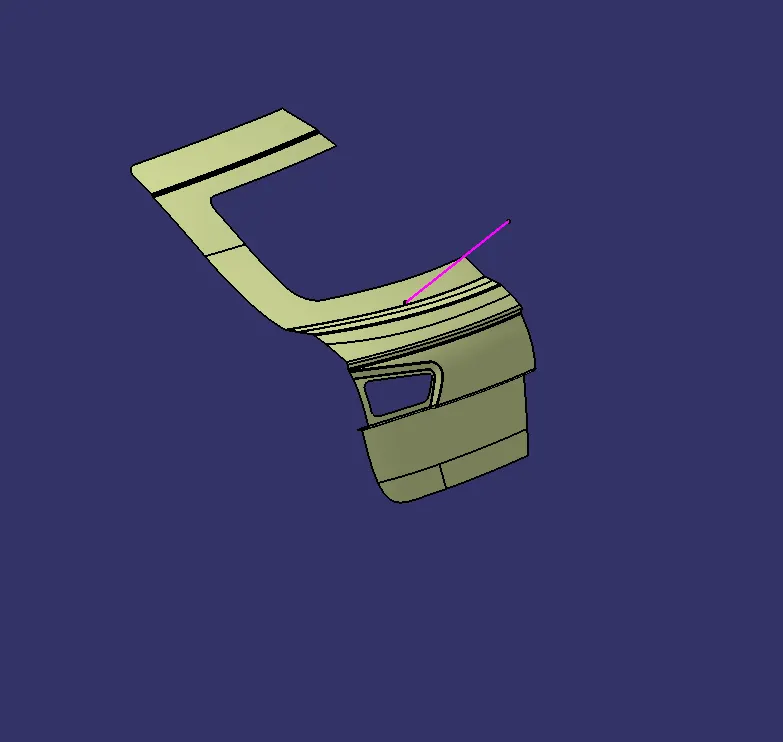
-Next is create a tooling direction for the drawing direction which will be followed in most parts for draft analysis and that will help in conforming manufacturability of the part.
Step-4
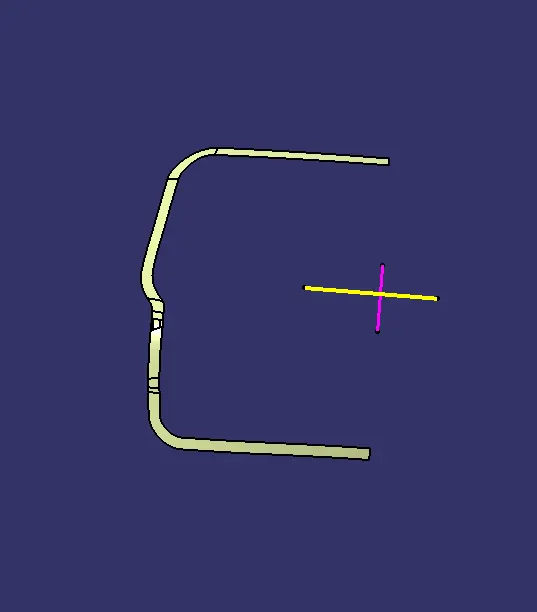
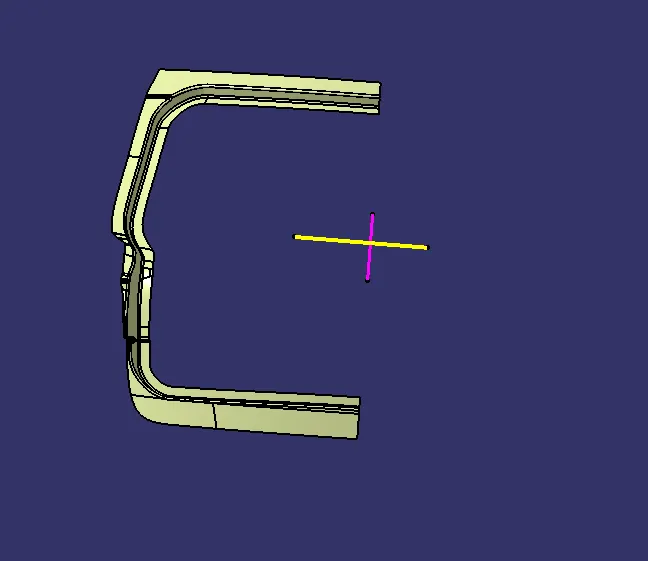
Now for creating a sealing flange for the back door on the inner panel we should offset outer panel acccordingly. For Inner panel it would be offset of outer panel with the thickness considerations for both inner, outer, reinforcement and hemming flange.
Step-5
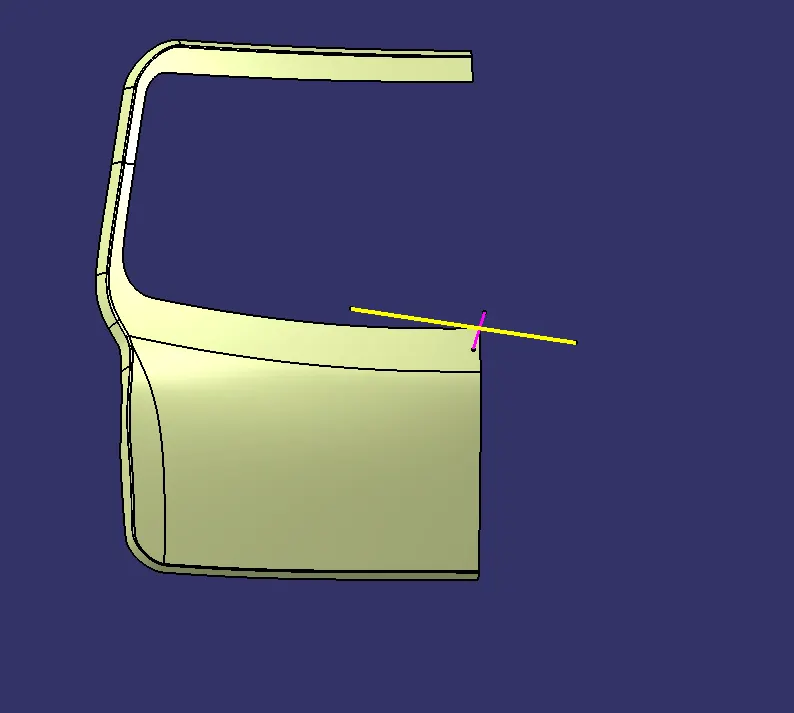
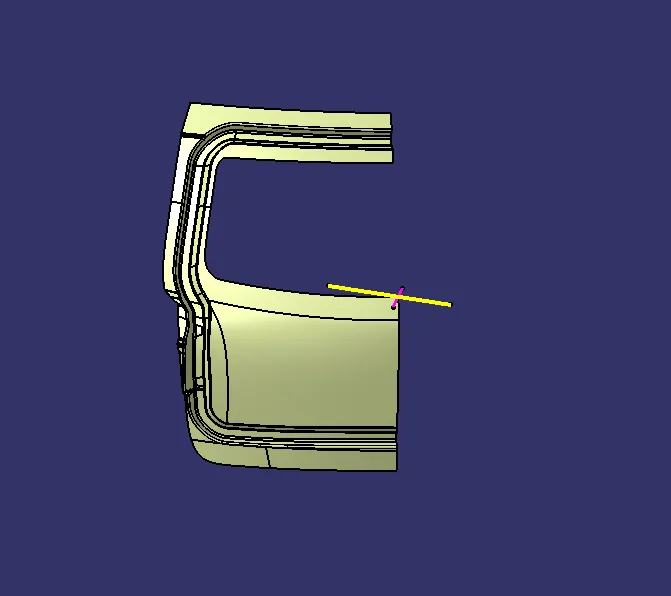
Next will be creating Wind Sheild Panel for the mounting of wind Sheild which will be created on the inner panel by taking reference from the outer panel .
Step-6
- After will be the creation of embosses following the force dissipation which create embosses in Y or V direction which will reduce collision impact.
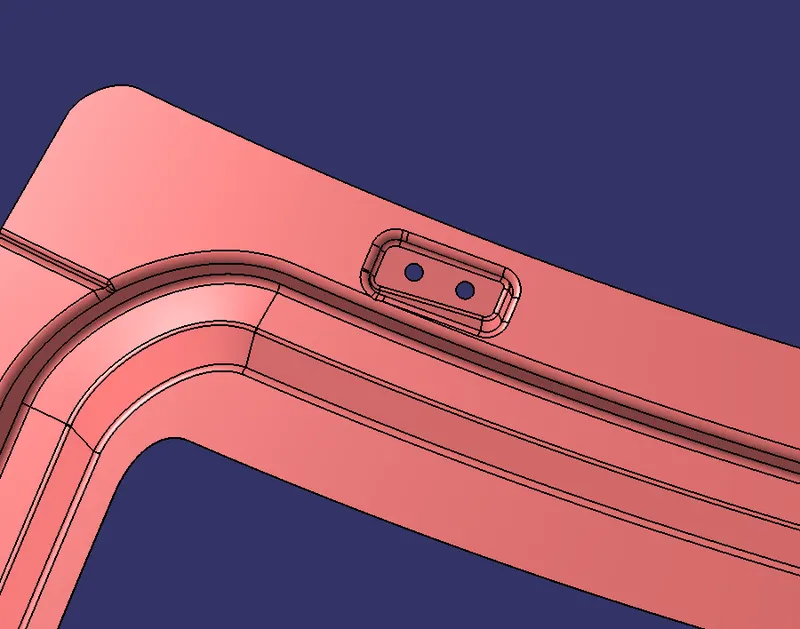
- Also Creation of Hinge Emboss, Gas Stay Embosss, Wiper Emboss and Latch Striker emboss.
- There is another flange which will be created from the inner panel and wiil be joined with the outer panel with the mastic filling having appropriate gap of 5mm which will reduce vibration on the back door.
Step-7
Hinge Emboss And Reinforcement:
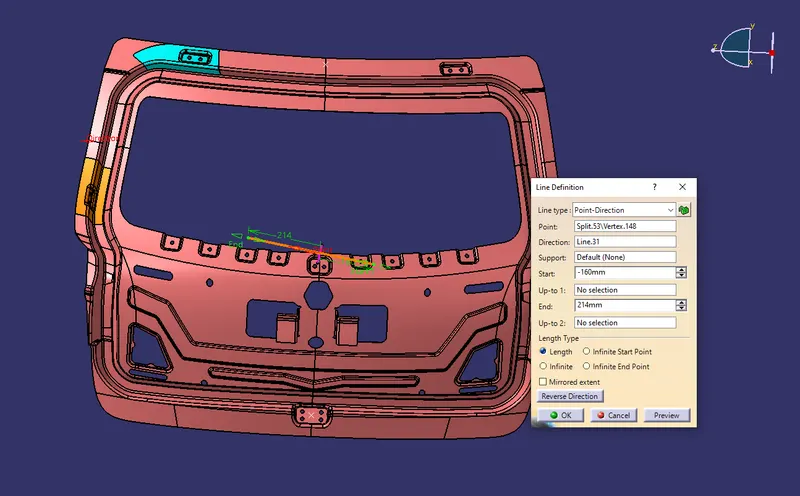
Hinge embos is created on a tentative position so that from hinge axis center point we could create a trajectory for which will be perpeniducular to striker at its local area that will help us creating Latch and striker emboss also positing of it.
Latch And Striker Emboss:
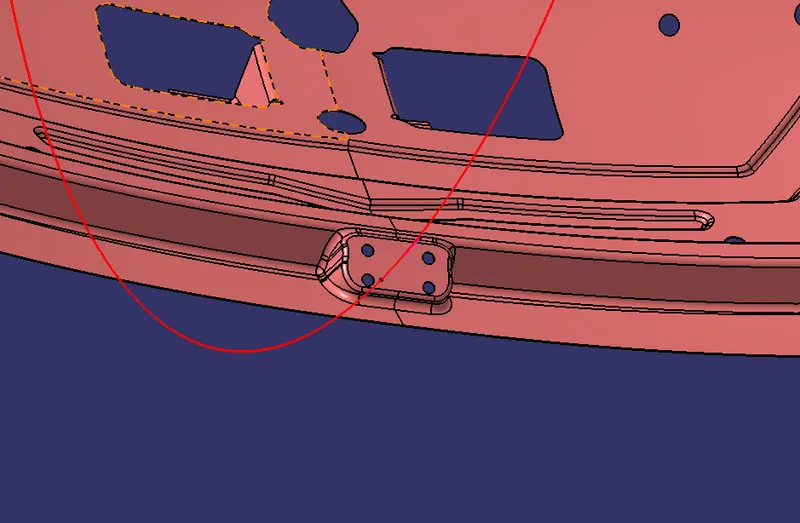
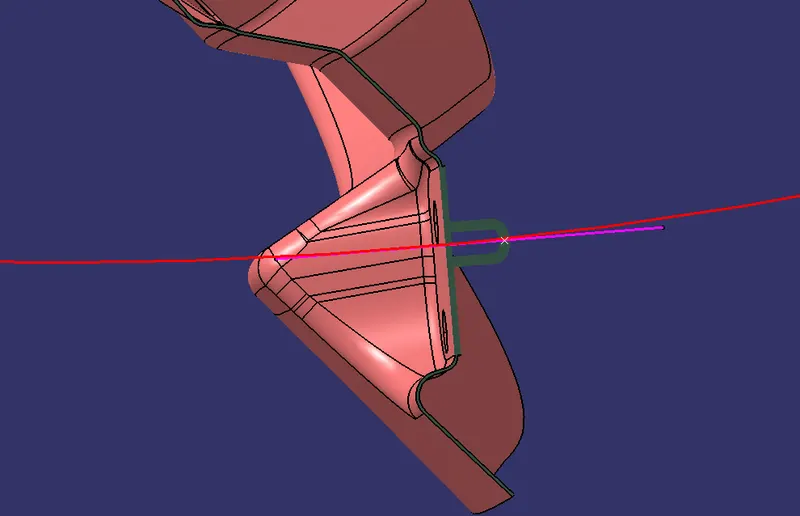
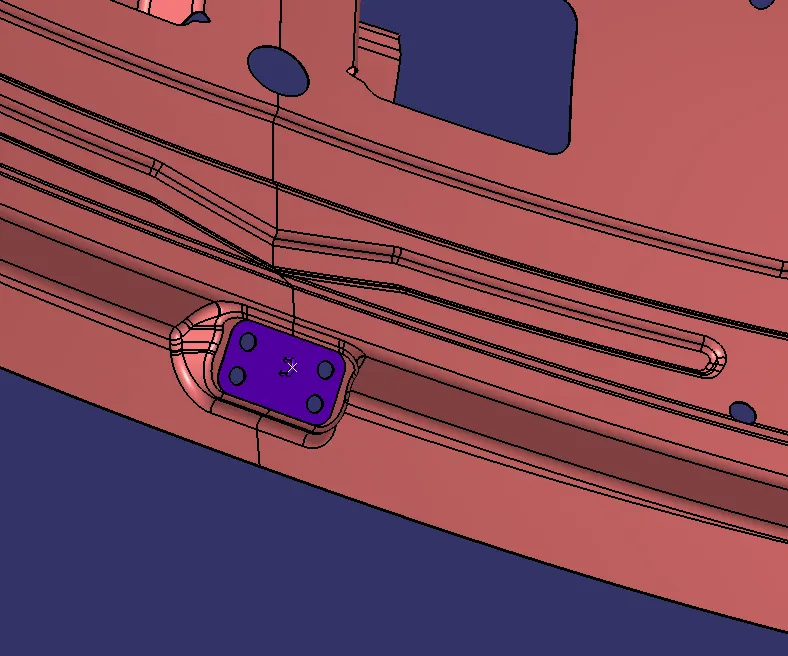
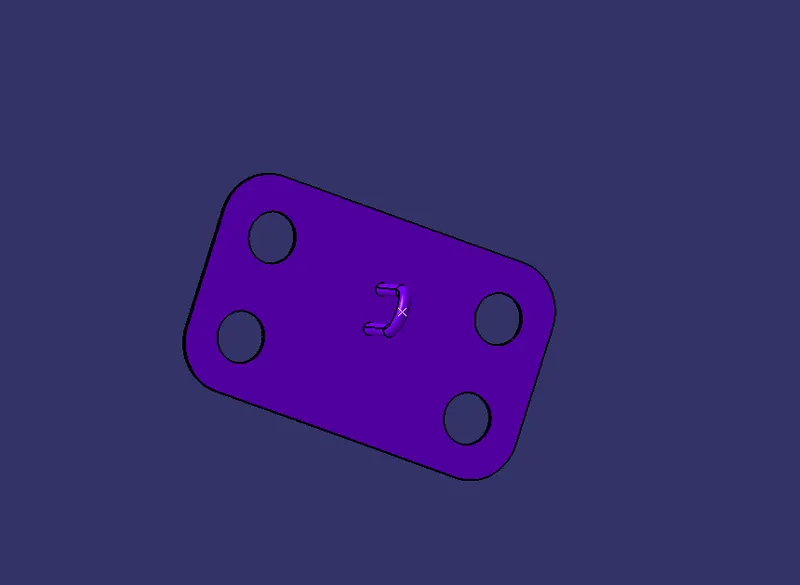
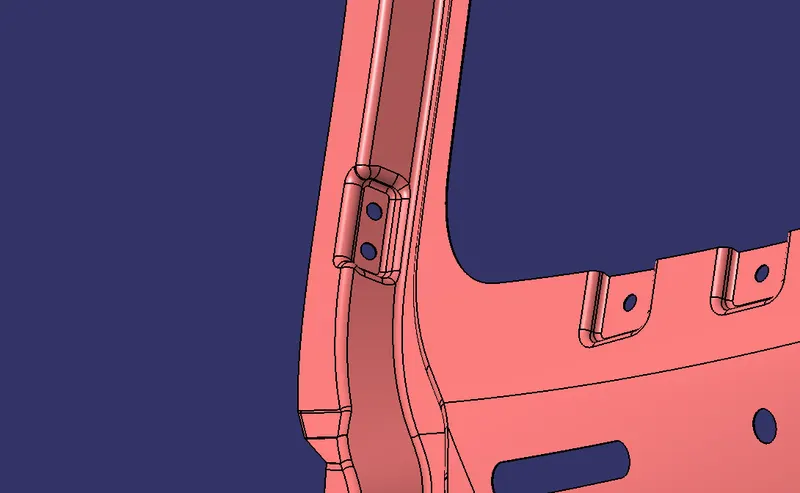
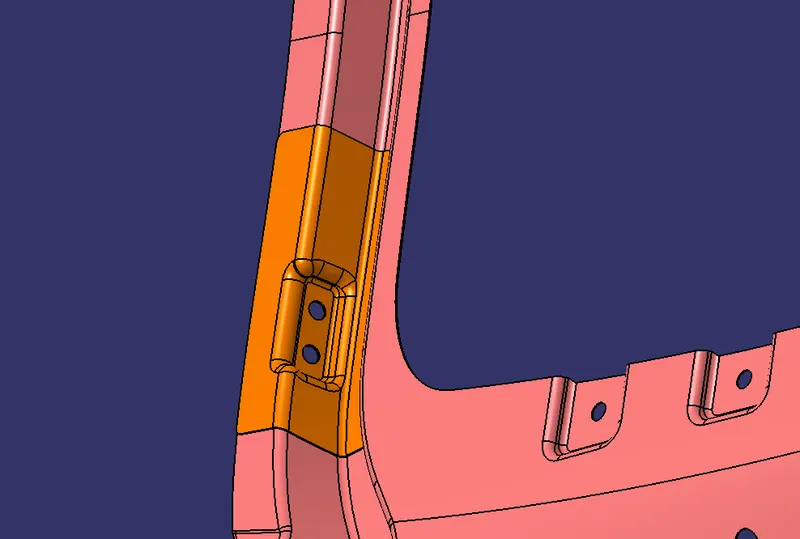
Gas Stay Emboss And Rein Forcement:
- It is a position where gas stay will be mounted in a such way that it can stay in position when lifted open.
- Here i have created different tooling axis for the emboss from main tooling axis for my part.
Wiper Motor Emboos And Reinforcement:
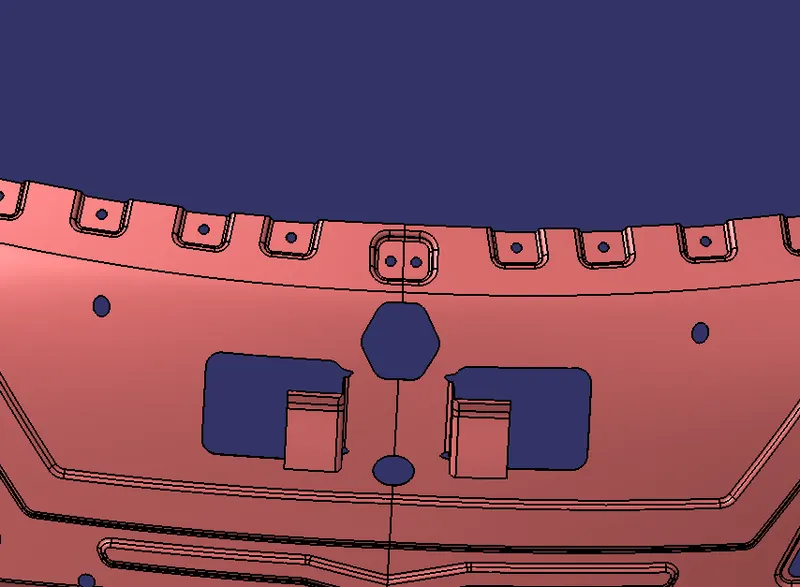
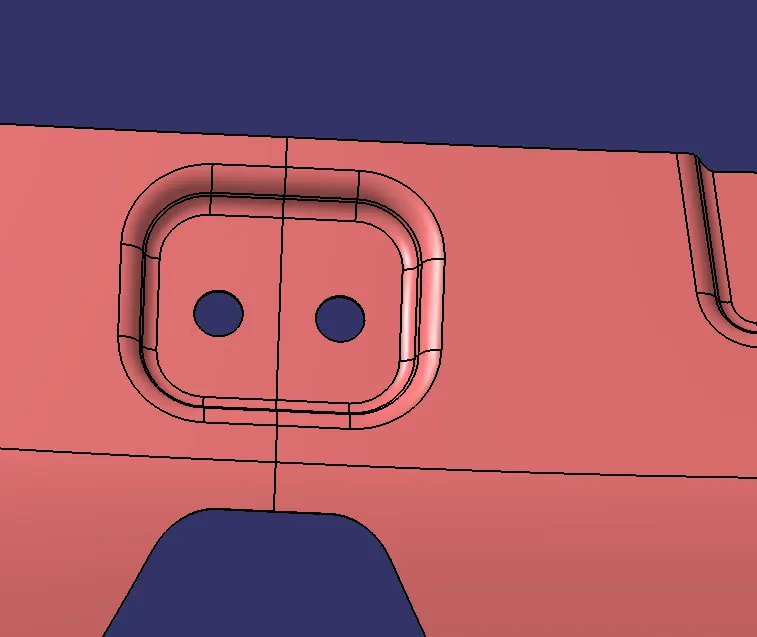
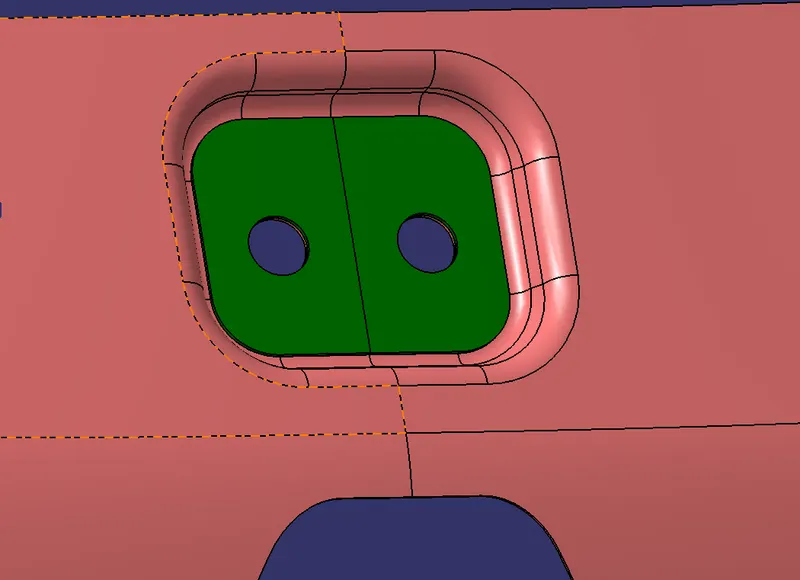
Step-8
- Hemming And Hemming Relief on the Outer panel with consideration of thicknes of the parts and hemming flange length which should be Min 3mm and Max 6mm. Also maitaining gap atleast of .2mm between parts.
Step -9
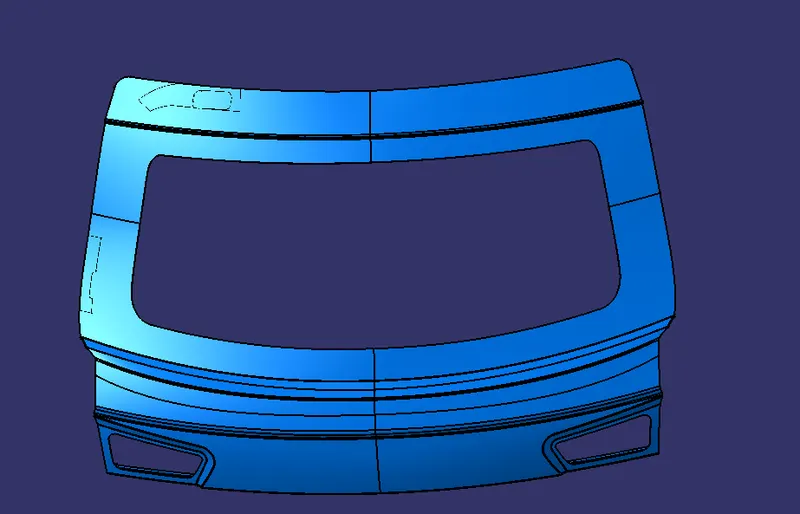
Assembly of Back Door:
Step-10
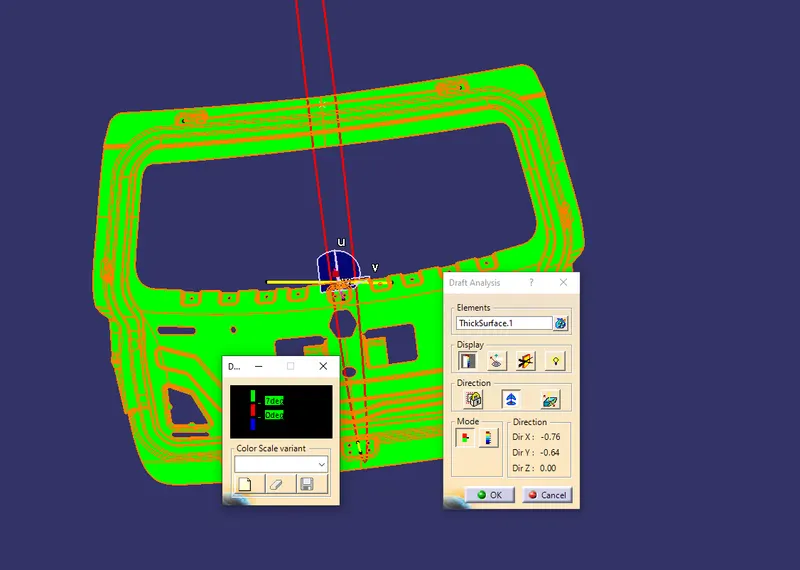
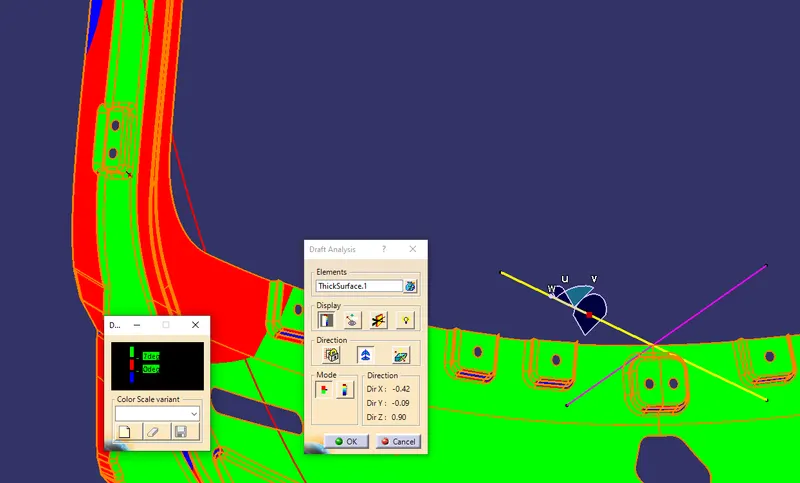
Draft Analysis :
- For draft analysis the min draft angle should be 7 degree in sheetmetal.
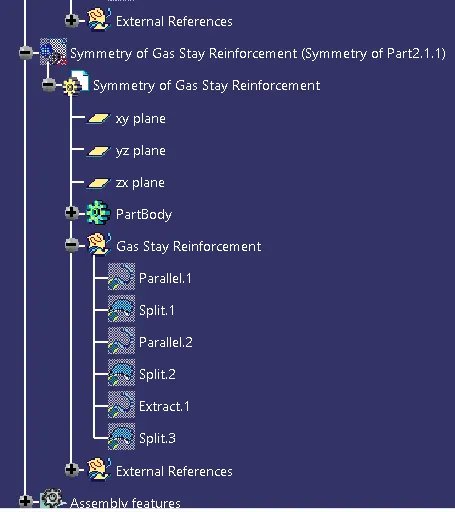
TREE STRUCTURE
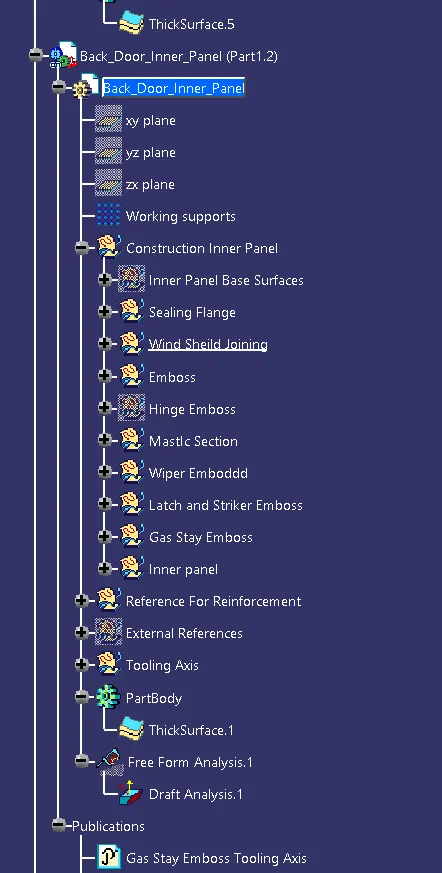
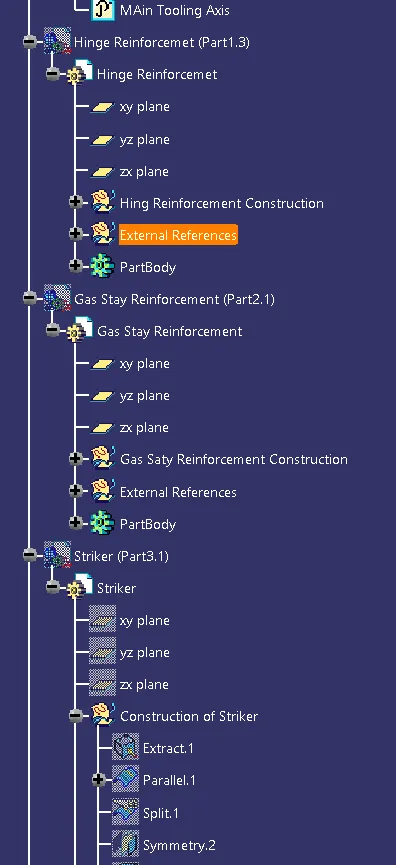
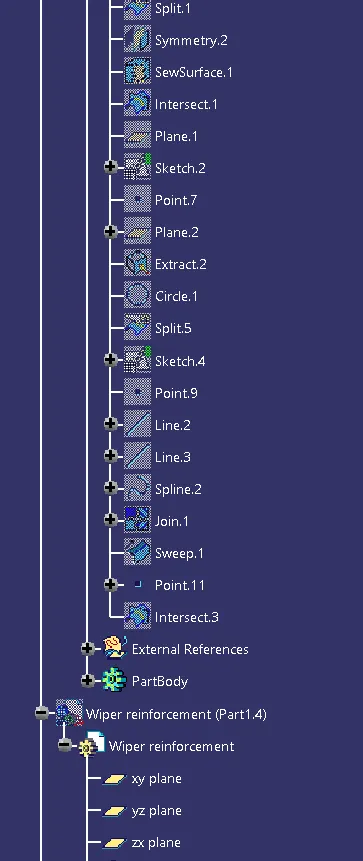
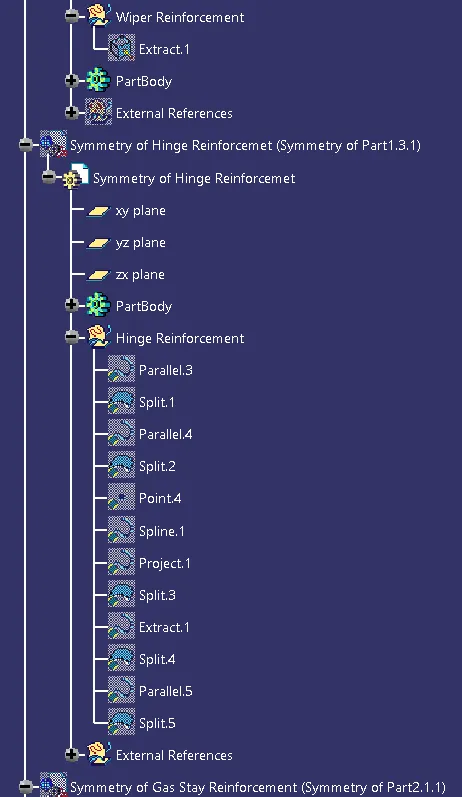
CONCLUSION
As per given surface we compeletd designing Back Door with all the Design considerations.