The Basics of Mold Design: Wrapping up the DFM List
We have thoroughly reviewed the DFM checklist in previous articles on the basics of mold design using SolidWorks. In this article, we will complete the list and cover the basic principles of:
 Navin Baskar·16 Dec 2022·4 min read
The Basics of Mold Design: Wrapping up the DFM List
We have thoroughly reviewed the DFM checklist in previous articles on the basics of mold design using SolidWorks. In this article, we will complete the list and cover the basic principles of:
- Balancing
- Gate location
- Flow leaders
Balancing in Mold Design
The pressure of the injected material in the mold is very high, and proper clamping should be provided to eliminate any defects when injection molding takes place.
The clamping force provided by a machine of a specific tonnage exerts and an equal amount of pressure on all the ends of the machine.
Case 1
In the image below, the diagram on the left is the side view of the mold, which shows the runner, cavity, and mold block. On the right side, you can see the same mold block in an isometric view with all the forces acting on it.
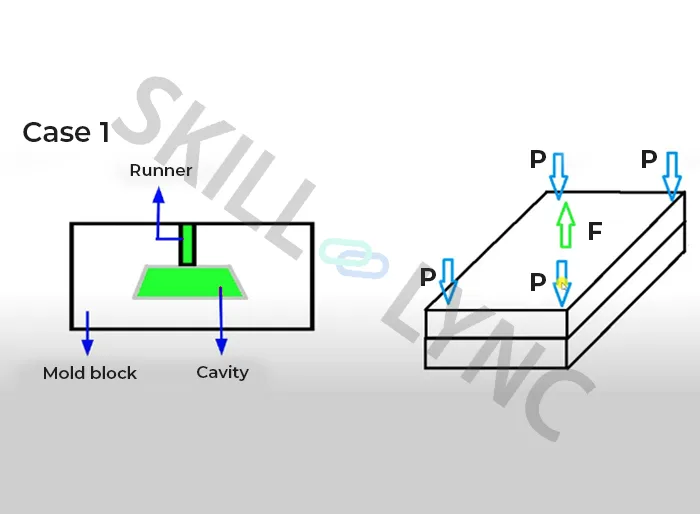
In the first case, you can see that the runner is at the center of the mold. So, when the molten material is injected into the mold, there will be a force at the center of the mold blocks, which will try to separate the mold blocks from each other. This force is denoted by the letter 'F' in the diagram.
Since the mold blocks should not get separated, an equal clamping force will be exerted on all ends to counteract the pressure of the molten plastic. This clamping force is denoted by the letter 'P', and its values are calculated based on the same formula used for calculating the tonnage of the machine.
Since the clamping force balances the opposing force at the center at the ends, the first mold is said to be 'balanced' and will function properly.
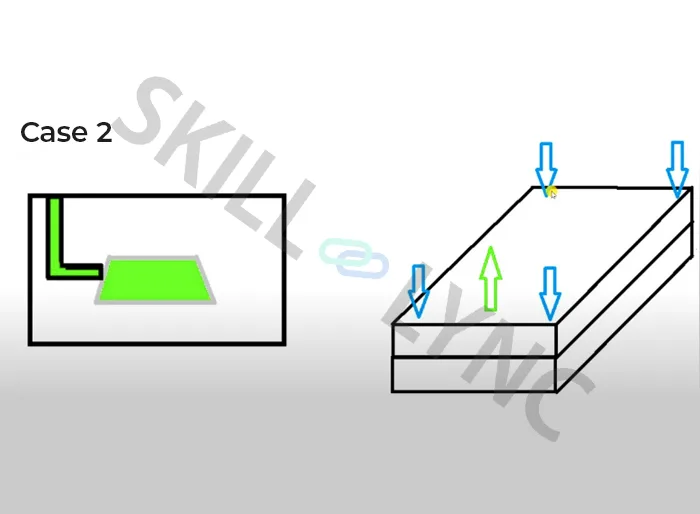
Case 2
If you cannot provide the gate's location at the top or center, you would have to add it on some other face.
If you provide a runner, as shown in the diagram below, then the point at which the injected material creates an opposing force will also change. It will be near the ends, as shown in the diagram to the right of the image below.
Now, as the opposing force is not at the center, one side of the mold will require a higher clamping force than the other side. Since it is impossible to have different clamping forces at each end, there will be some points in the mold where the clamping force is too high or too low. Such a case is known as an unbalanced mold, and it cannot be used.
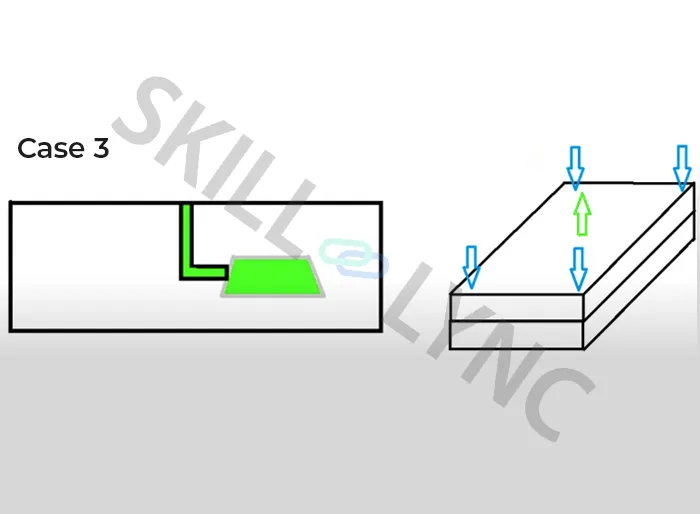
Case 3
In this case, you can see that the size of the mold block itself is increased to keep the sprue at the center. So, the molten material injected will exert an equal force on all ends, and the clamping force will also be uniform. Hence, the mold will be balanced.
Takeaway
What's important to note here is that the sprue location should always be at the center of the mold.
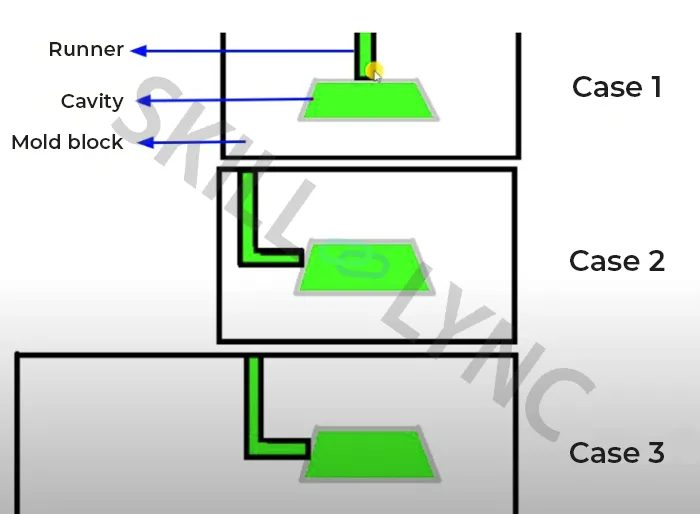
So, for single cavity tools, you should go for case 1 as it is balanced. The material cost and runner length are also less in this case. But if you are unable to opt for Case 1 due to gate location constraints, then you would have to go for Case 2.
In the case of multiple cavity tools, you would inevitably opt for Case 3. You can even add a second cavity to the same mold and have a two-cavity mold.
Gate Location in Mold Design
If your part has a slot in the center, you can place the gate's location at the center (blue arrow in the image below), rather than outside the part (red arrow).
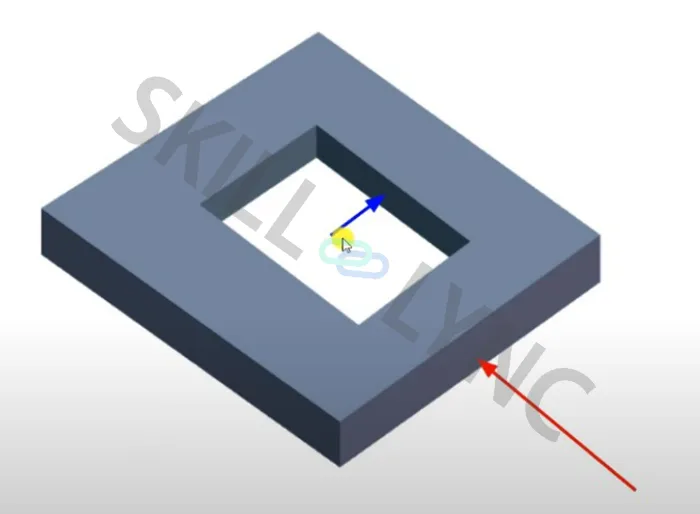
The blue arrow case is similar to the first case of balancing, and the red arrow to that of the third case in the balancing section.
So, providing the inlet from the center will reduce the runner channel's length and help in reducing the costs of runner channels and also reduce material wastage.
Better Surface Finish and Higher Drafts on Cavity Side
Another point to note is that, generally, a better surface finish will be given on the cavity side compared to the core side.
Also, the draft angles on the cavity sides are more than the core ones. This is done to ensure that the plastic does not stick to the walls of the cavity.
When the core moves away from the cavity, the part should come along with the core where it is ejected using the ejection pins. It should not stick to the cavity's walls when the core plate moves back or retracts.
To prevent the part from sticking to the cavity, you must provide a better surface finish and higher drafts on the cavity side.
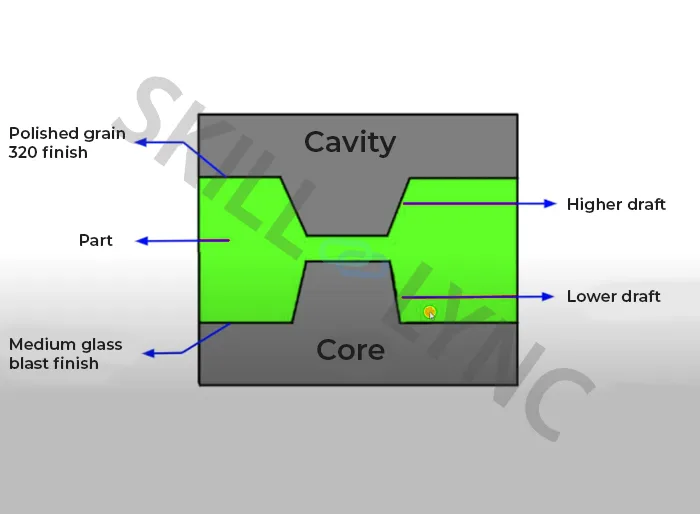
In the above image, the 'polished grain 320' and 'medium glass blast' are surface finishes. The polished grain finish is a better surface finish compared to the glass blast.
Flow Leaders in Mold Design
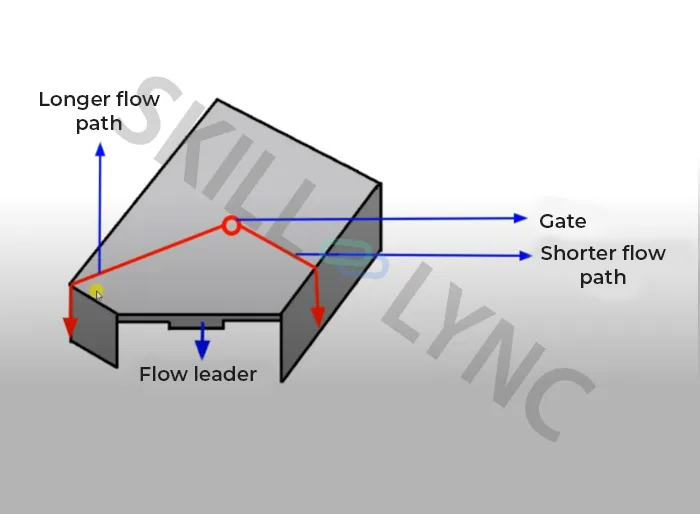
In the above image, if you provide the gate's location at the center, you can see that some regions of the mold will fill earlier compared to other areas. The walls closer to the gate point will be filled first, and the walls farther will be filled later.
You can make flow leaders achieve a uniform flow over the part.
Flow leaders are specific regions in a part that are purposely made thicker to promote the flow of the material. The flow of the feed material will increase in areas of higher thickness, which will help achieve an overall uniform flow of the feed material.
Click here for more information on job-leading engineering courses.