Project 1 Mechanical design of battery pack
Aim:
To design a Mechanical Design of Battery Pack using the cell- ANR26650M1-B
Objective:
- To create a battery pack drawing of 18KWh using Series and parallel connections of battery modules made up of individual Li-ion cells.
- Li-ion cell used here is ANR26650M1-B
To discuss about the enclosure used for battery pack.
Introduction:
Details of Battery:
Nanophosphate Technology 26650 Lithium Ion Power Cell
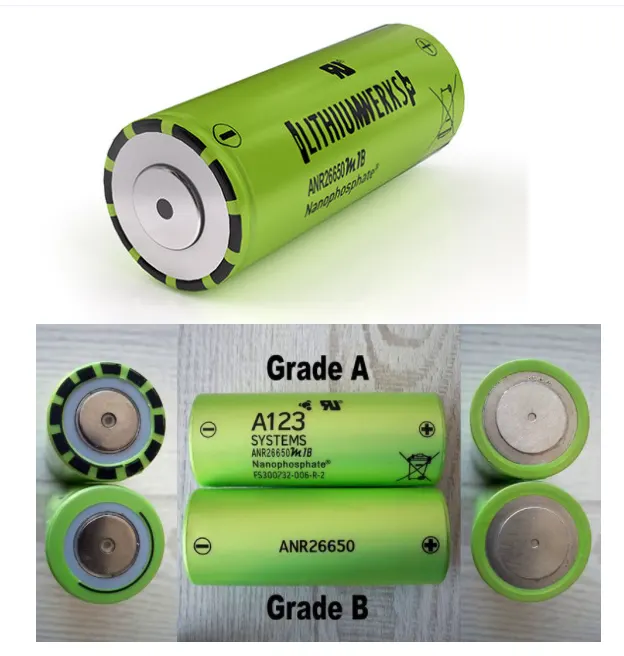
Lithium Ion 26650 cells are capable of delivering very high power due to its use of patented Nanophosphate battery technology Based on Lithium iron phosphate
26650 Lithium Ion Battery Definition:
26650 is a cylindrical lithium battery specification. 26650 battery is applicable to special equipment, medical equipment, instruments, power tools, logistics, security monitoring, exploration and mapping, etc.
26650 lithium battery dimension: The diameter is 26mm, and length is 65mm.
26650 Lithium Ion Battery Advantages:
26650 lithium battery has high energy density, low self-discharge rate, stable charging and discharging performance, no memory effect, no decomposition in heat, high safety performance, long life cycle and high voltage. You can connect 26650 lithium battery in series or in parallel. It is environmental friendly and has no pollution.
- High energy density: theoretical specific capacity 170mAh/g, actual specific capacity ≥140 mAh/g (0.2c, 25°C);
- High safety: the most secure positive electrode material for lithium ion batteries;
- No pollution: does not contain any heavy metal elements that are harmful to human body;
- Long cycle life: it can charge and discharge more than 2000 times under 100%DOD;
- Fast charging performance: Lithium iron phosphate battery can be charged at high rate
26650 lithium battery materials are mainly divided into ternary materials and lithium iron phosphate materials.
- Voltage
INR26650 lithium battery has nominal voltage of 3.6V, full charge voltage of 4.2V, and discharge cut-off voltage of 3.0V.
IFR26650 lithium battery has nominal voltage of 3.2V, full charge voltage of 3.65V, and discharge cut-off voltage of 2.0V.
- Capacity
IFR26650 lithium battery capacity includes 2800mAh, 3000mAh, 3200mAh, 3400mAh, 3600mAh, 3800mAh and 4000mAh.
INR26650 lithium battery capacity tends to be 4500mAh, 5000mAh, 5500mAh and 6000mAh
26650 Lithium Ion Battery Positive Electrode Materials
26650 lithium battery positive electrode materials include lithium cobalt oxides, lithium manganese, NCA, NCM and lithium iron phosphate. Material system determines the working voltage and single cell capacity. Various materials manufacturers and cell manufacturers improve the overall indexes, such as battery voltage and capacity, by special material adding, coating process and manufacturing process improvement. Working voltage and theoretical capacity of various materials are normally as follow:
- Lithium cobalt oxides 3.6V, theoretical capacity 274mAh/g
- Lithium manganese 3.7V, theoretical capacity 148mAh/g
- Ternary material 3.65V, theoretical capacity 278mAh/g
- Lithium iron phosphate 3.2V, theoretical capacity 170mAh/g
- The materials determine the cycle life of the battery, so does the manufacturing level of the battery manufacter
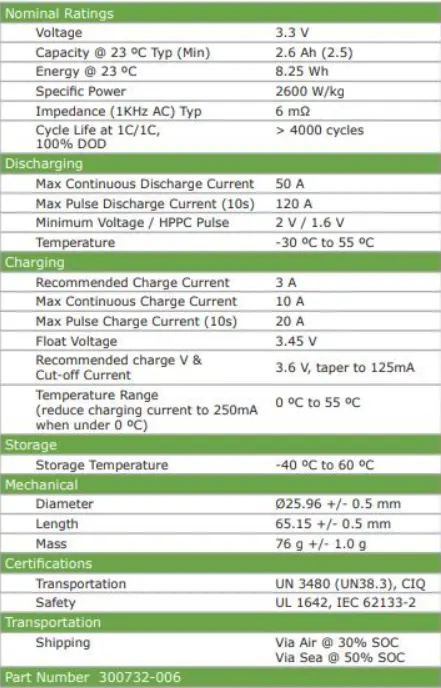
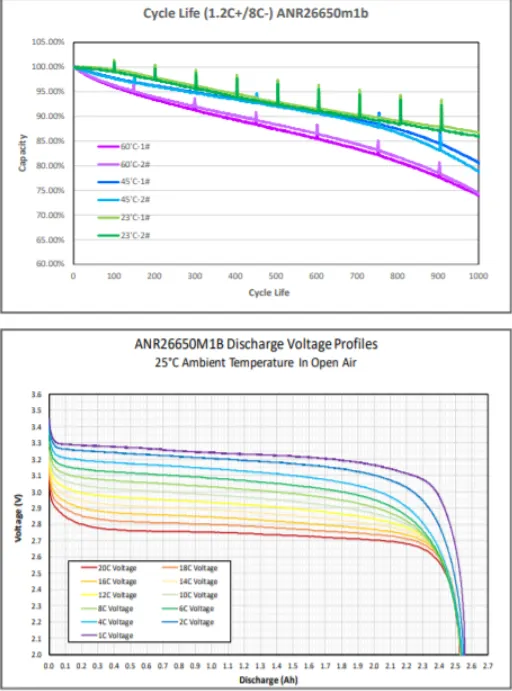
Cell Specification:
Discharge Voltage Profile and Cycle life with respect to different Operating temperature from datasheet
Energy Required=18kWh.
Number of cells(N)= Energy/(nominal voltage* Capacity)
N= 18000/(3.3*2.5)
N =2182
The minimum cell 2182 is required to get 18kWh energy. When the cells are connected in series the capacity remains the voltage will be the sum of each individual voltage. In parallel connection the voltage remains the same and capacity accumulates.
Nominal voltage of one cell = 3.3v.
Number of cells required to be connected in series connection to produce 330V and the capacity of the module will be 2.5Ah.
Ns(cell in series) = 330/3.3
Ns=100
To find the number of cells connected in parallel.
Np(cell in parallel) = total cell /Ns
Np =2182/100
Np= 21.82
cell architecture = 100S22P where 100 cells in series and 22 cells in parallel.
Battery Capacity:
Capacity = Parallel cell row* individual cell capacity.
Capacity=2.5*22
Capacity = 55Ah.
Current Supplied by the battery:
We have already calculated battery capacity which is 55Ah means it is going to supply 55A current per hour.Which can be Considered as C-rate
Range:
Powertrain energy consumption = 129 Wh/Km at 70% powertrain efficiency.
Range = capacity/ energy consumes per Kilometer
Range= 18000/129
Range =139 Km.
Internal Resistance of Battery:
The entire resistance encountered by a current as if it flows through a battery from the negative terminal to the positive terminal is known as internal resistance of battery.
Battery dimensions:
The below diagram shows where to find width, height and length
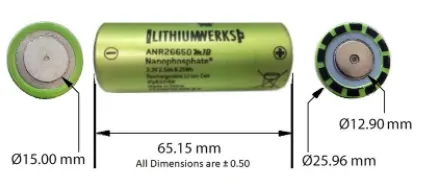
ANR26650M1-B cell has 26mm diameter and 65mm height.
Length of casing(L) = number of cells at mid*(cell diameter(26)+ margin at both side of cell(4))+clearance at side(diameter of edged cell + margin)
L = 98*30+60
L = 3000mm
Breadth of casing(B) = cell diameter(26) + margin at both side of cell(4) + clearance at side(diameter of edged cell + margin)
B = 20*30+60
B = 660mm
Height of casing(H) = 65 + 35 (Height of cell + margin for the cell holder and metal strips)
H = 100mm.
Weight of battery pack:
cell weight = 76g.
Number of cells = 2182.
Battery pack weight(W) = cell weight * number of cells+ weight of accessories.
W = 76*2182+4.5
= 165.8+4.5
=170.3Kg
Materials and process in battery pack construction:
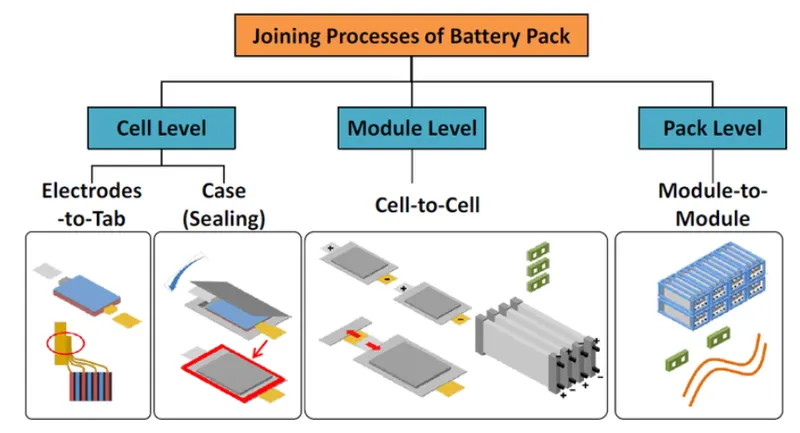
Joining Technologies of cells:
The interconnections between cells/modules are practised by Various welding techniques. Some of them are
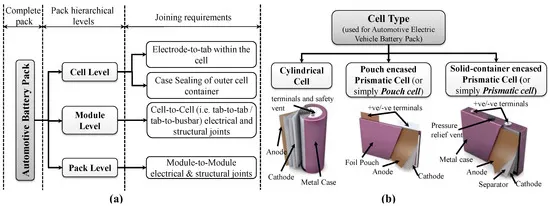
Overview of Key Joining Challenges
-
Electrical and thermal challenges: (i) Producing joints with low electrical resistance—lower electrical resistance at the joint results in low energy loss, low heat generation, and subsequently, lower joint temperature increase during charging and discharging. (ii) Producing joints with low thermal input—low thermal input is preferable, especially when joining with fusion type welding processes, as exposing the cell to high heat may melt or disturb the safety vent, compromise seals, or cause internal shorting. (iii) High thermal fatigue resistance—thermal fatigue resistance of battery interconnects is an important criterion for long-term durability and reliability performance.
-
Material and metallurgical challenges: (i) Compatibility for dissimilar materials joining—dissimilar materials may create intermetallic layers, which are not preferred because of their higher electrical resistance and brittle nature compared with parent materials. Therefore, joints with low intermetallic is preferable. (ii) Variability of materials and surfaces—highly conductive and reflective materials, any surface coatings or oxide layers, joint stack-ups (especially varying thicknesses and/or multiple sheets) also need to be overcome for satisfactory joints.
-
Mechanical challenges: (i) Durable joint strength—the joint area/nugget size that can be achieved by the joining methods should have satisfactory joint strength with low strength variability. (ii) Avoid mechanical and vibrational damage when joining—excessive deformation of, or transmission of vibration into, the cell may damage internal connection. Precautions must be taken to avoid these as induced residual stress or vibrational energy may be released and cause joint failure.
Major and Emerging Joining Technologies:
- Ultrasonic Welding or Ultrasonic Metal Welding (UMW)
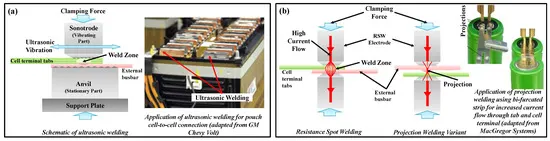
- Resistance Spot/Projection Welding
- Micro-TIG or Pulsed Arc Welding (PAW)
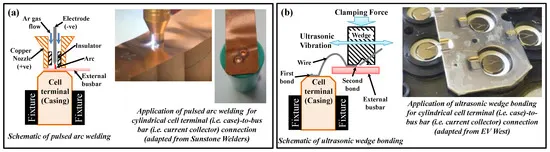
- Ultrasonic Wedge Bonding
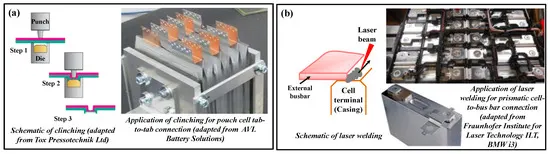
- Micro-Clinching
- Soldering
- Laser Welding
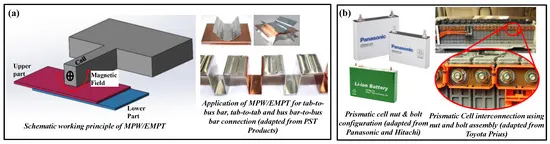
- Magnetic Pulse Welding (MPW)/Electromagnetic Pulse Technology (EMPT)
- Mechanical Assembly
Battery Pack Hierarchical Joining
- Joining of Cylindrical Cell Based Battery Pack
-
Cell level joining: The assembly process for cylindrical cells requires joining methods at two levels, which are (i) electrode foil-to-tab joining and (ii) terminal welding (i.e., tab-to-case/can). Ultrasonic and resistance spot welding are the most commonly used joining methods for electrode foil-to-tab and terminal welding, respectively . Laser welding is also feasible for electrode foil-to-tab joining, however, tight part-to-part tolerance has to be maintained for satisfactory joints. Terminal welding is not be feasible by laser welding if line of sight is obscured.
-
Module and pack level joining: Because of the physical size and form of a cylindrical cell, external current collectors are added to connect cells. Physical projections reduce the contact area in projection welding, allowing concentrated heat generation at the point of contact, and formation of the weld nugget faster and at a lower current level compared with conventional spot welding , reducing potential damage to the RSW-electrode. Similar to resistance welding, advances in high-frequency power supplies, increased low-current control, and arc stability, have enabled much finer TIG welding, such as pulsed arc welding. Pulsed arc welding offers excellent copper to copper joining with a fairly relaxed process window with respect to part fit-up and positioning tolerances of the electrode to the parts . As ultrasonic welding exerts high frequency vibration under locally applied force, there is a risk that a cell may suffer internal damage to the electrode. Therefore, ultrasonic welding of cylindrical cells at module level may not be appropriate without steps to mitigate the possibility of damage. However, ultrasonic wedge bonding has been used for cell-to-cell connections. In the Tesla battery pack each of the cells has two wires that act as fuses (one each for the anode and cathode) and are connected using ultrasonic wedge bonding. Laser welding is emerging as an efficient alternative for forming joints between cylindrical cell terminals and external current collectors, that is, bus bars. However, part-to-part fit-up needs to be carefully controlled to achieve satisfactory joints using laser welding. By designing proper jigs and fixtures, a large number of cylindrical cells can be connected to produce a battery module. Permanent joining, such as welding, may not be suitable for large pack level joining because of battery maintenance and service requirements As a consequence, mechanical nut and bolt assembly has been widely adopted at the pack level.
- Joining of Pouch Cell Based Battery Pack
-
Cell level joining: During fabrication of pouch cells, the joining operations are (i) electrode current collectors to positive and negative terminal tabs, and (ii) case sealing of pouch cell—an automated and standard process under vacuum . Electrode-to-tab welds are conventionally made using ultrasonic technology because of the need to create a joint through a stack of foils. RSW is not appropriate as RSW-electrodes are prone to picking-up highly conductive cell terminal/electrode and tab materials . However, fibre laser welding technology may be used for increased weld quality and strength . The key to successful application of laser welding is to ensure that (a) the foils are in close contact, and (b) a pulsed laser is used to avoid overheating. In the case of pouch cell case sealing, typically, a compact heat sealer is used to seal aluminium–polymer laminate films.
-
Module and pack level joining: Module designs typically position positive and negative terminal tabs either at opposite ends or the same end of the cell based on series or parallel connection requirements. Therefore, the cells are joined either by tab-to-tab or tab-to-bus bar connections. Ultrasonic welding has received significant attention for module level joining as a result of its ability to produce good welds for dissimilar materials and multiple thin layers. RSW or projection welding, pulsed arc welding, and clinching of tab-to-tab or tab-to-bus bar joints are feasible. However, process stability, joint characteristics, thermal input, and process control require further investigation. However, feasible soldering of pouch cell interconnects is not recommended as it raises concerns of joint strength under vibration, neutralisation of fluxes, risk of localised heat damage, and creation of debris in the joint area. As an alternative, MPW/EMPT has the potential for joining pouch cell tab-to-tab or tab-to-bus bar . However, detailed investigation is required for MPW/EMPT application, as induced eddy currents may affect the physical parts/electrochemistry (e.g., potential cracks or internal joining between current collectors that leads to battery internal short-circuit) of the pouch cell. To mitigate the risk of damaging the pouch cell, or module sensors, a specially designed weld head and shielding plate may be required during EMPT welding. Laser welding is another alternative solution for pouch cell tab-to-tab or tab-to-bus bar joining. Fibre lasers are able to weld many material combinations including aluminium to aluminium, aluminium to steel, copper to steel, and copper to aluminium. Further investigations are required for fixture design, process parameter optimisation and process control. Generally, pack level (i.e., module-to-module) connections are made with mechanical fasteners.
- Joining of Prismatic Cell Based Battery Pack
-
Cell level joining: The fabrication of prismatic cells involves similar joining operations to cylindrical and pouch cells (i) between current collector tabs and electrode foil(s), (ii) between collector tab and battery terminal, and (iii) case sealing. Ultrasonic welding is most commonly used for joining current collector tabs with electrode foil(s) . Resistance spot welding is used to connect current collector tabs with the case or with the top cap of the case . Typically, prismatic cell positive and negative terminals are based on mechanical nut and bolt assembly. Laser welding is also used for cell level joining and traditionally case sealing. As reported by Shannon , laser welding has potential for a number of manufacturing applications, such as case sealing and terminal welding.
-
Module and pack level joining: As a result of the stackable form of prismatic cells, battery pack modularity and various design configurations for parallel or series connections are readily achievable. Module and pack level joining is mainly performed with mechanical nut and bolt fasteners or clip fitting. Mechanical nut and bolt assembly has the advantage of easy disassembly and higher joint strength compared with other reported joining techniques. However, there are issues with high contact resistance and maximum torque (to avoid internal damage) that can be sustained by the cell stud. In some cases, laser welding has also been used for connecting cell terminal with bus bar . Ultrasonic wedge bonding and micro-TIG between terminal and bus bar may be feasible for prismatic cells. However, design changes may be required for UWB since cell terminals are not directly connected with bus bars. Application of these methods requires investigation of wire thickness, heat input, current carrying capacity, and so on.
Joining Technology Recommendation for Battery Manufacturing
Enclosure:
- Series Connection: Series connection is the connectivity of the components in a sequential array of components.
- Parallel Connection: Parallel connection is the connectivity of the components alongside to other components.
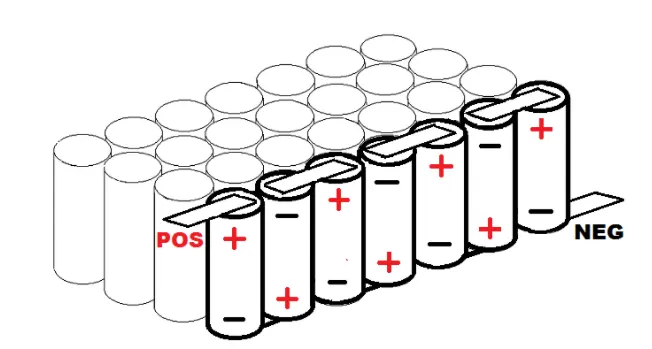
Cells in Series Connection
In series, cells are joined end to end so that the same current flows through each cell. In case if the cells are connected in series the emf of the battery is connected to the sum of the emf of the individual cells. Suppose we have multiple cells and they are arranged in such a way that the positive terminal of one cell is connected to the negative terminal of the another and then again the negative terminal is connected to the positive terminal and so on, then we can that the cell is connected in series.
Equivalent EMF/Resistance of Cells in Series
If E is the overall emf of the battery combined with n number cells and E1, E2, E3 , En are the emfs of individual cells.
Then E1 + E2 + E3 + …….En
Similarly, if r1, r2, r3, rn are the internal resistances of individual cells, then the internal resistance of the battery will be equal to the sum of the internal resistance of the individual cells i.e.
r = r1 + r2+ r3 + rn
Cells in Parallel Connection
Cells are in parallel combination if the current is divided among various cells. In a parallel combination, all the positive terminal are connected together and all the negative terminal are connected together.
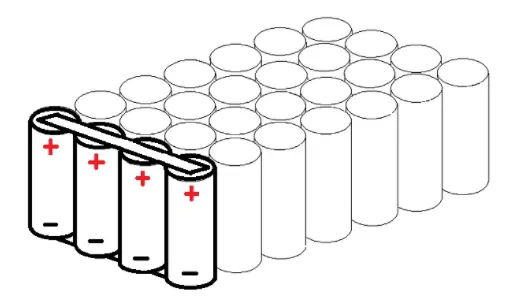
Equivalent EMF/Resistance of Cells in Parallel
r = (1r1 + 1r2 + 1r3 +…….. 1rn )-1
If emf of each cell is identical, then the emf of the battery combined with n numbers of cells connected in parallel is equal to the emf of each cell. The resultant internal resistance of the combination is above
Cell Holders:
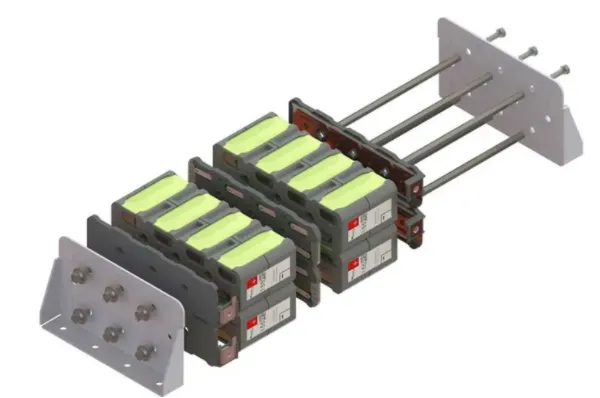
These houlders are used for houlding the individual cells in a better posture without mis-assemble.The connection can be made accordingly to make series connection and parallel connection to form the required module dimensions.
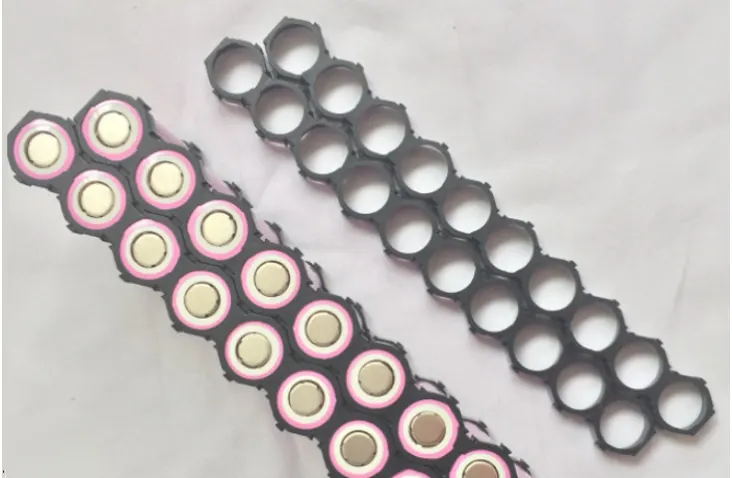
After installed the cells in a individual module the entire maximum positive and maximum negative terminal are made under Single pair of terminals as shown below
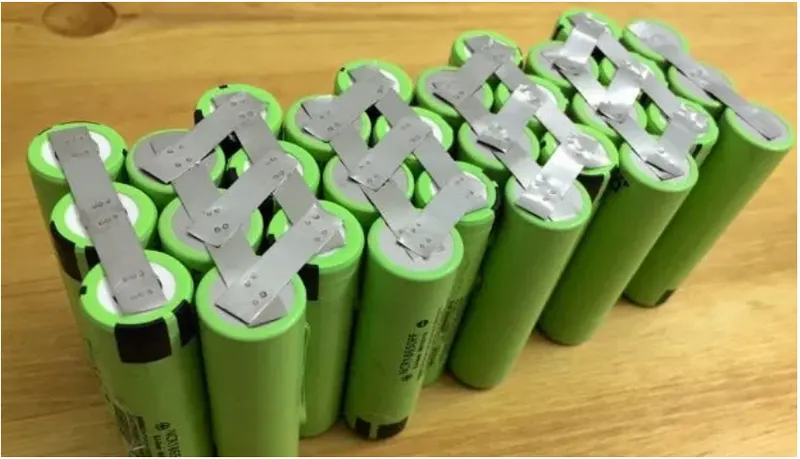
Here shown the cells are arranged and welded without using cell Holders as
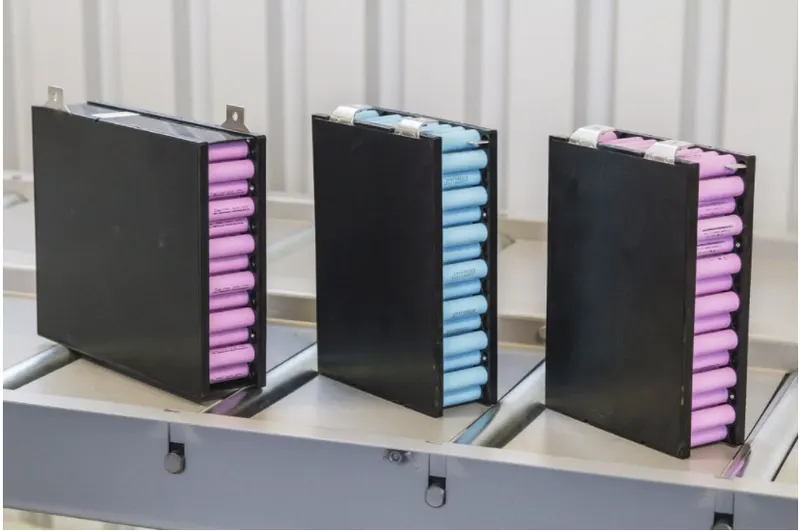
Battery pack arrangement:
Finally the overall battery pack after the arrangement of all cabinet connections with enclosure looks like this as shown below
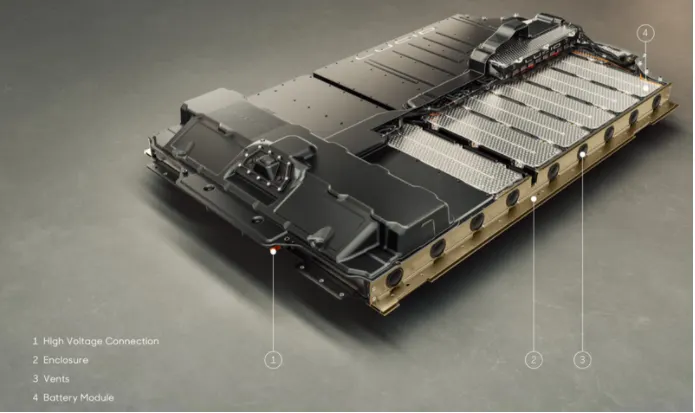
Vents holes are present with enclosure for cooling/ heating the battery pack temperature according to its environment conditions.
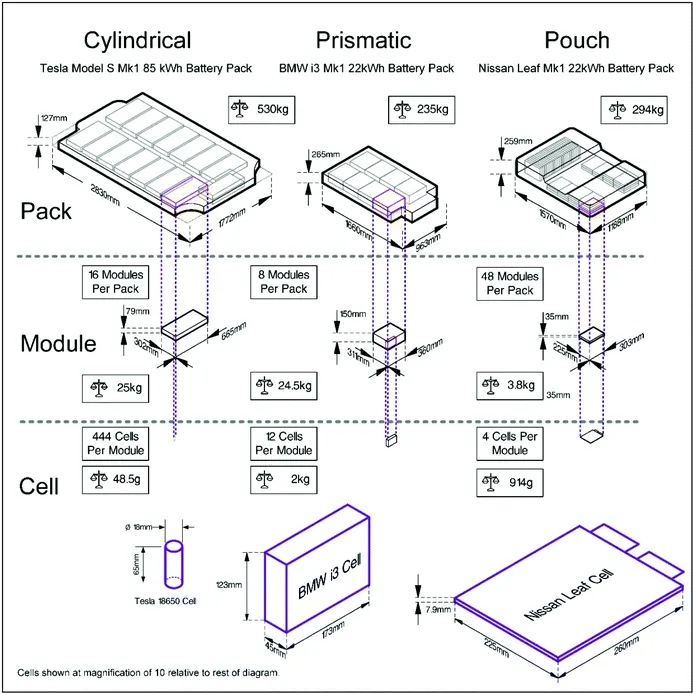
The pack construction are different for every Manufactures
Below shown battery pack construction types and process of Tesla, BMW and Nissan Leaf.
Conclusion:
- We design a Mechanical Design of Battery Pack using the cell- ANR26650M1-B
- Cylindrical, pouch, and prismatic cells, based battery pack construction are discussed in detail, with limitations of the specific technologies identified where their use is infeasible. Further, applicability of joining methods is discussed with hierarchical levels of battery manufacturing.
- Key joining challenges are identified for battery systems manufacture, including electrical, thermal, material, metallurgical, and mechanical challenges.
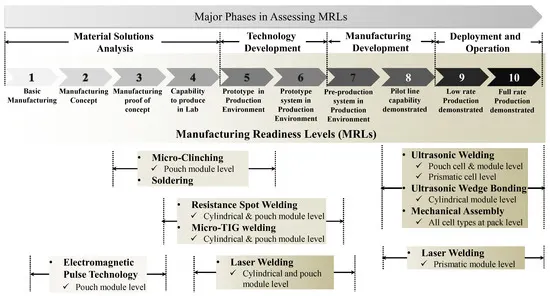
- Joining techniques are described with respect to MRLs and suitability of the identified joining technologies is quantified. Recommendations for further investigation of joining technologies are made based on Pugh matrix scores, MRLs, and application potential.