Design of backdoor
Aim :- The objective of this project is to design the back door of the car and make the inner panel for the back door and also design the necessary reinforcement and Embosses.
Introduction :-
- The back door of the car is one of the closure commodity of a vehicle which is present at the back portion of the car.
- While designing the back door space requirements are also taken into consideration as luggage room is also present in this region.
- The back door is a hinged door/tailgate at the rear of the vehicle. It may be used for loading and unloading cargo, or to get passengers in and out, in case there are seats present at the rear.
- The back door comprises of certain components which form the back door assembly together.
Types Of Back Door according to the Working Purposes :-
- Top Mounted Door
- Side Mounted Door
- Bottom Door
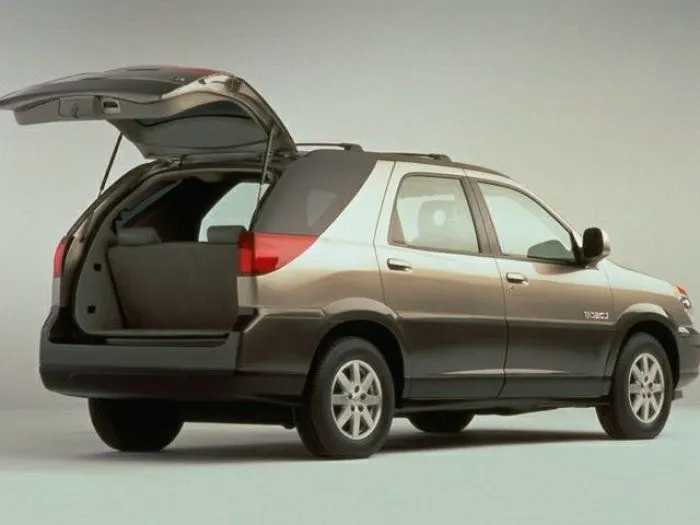
Generally most of the car comes with top mounted Back Door .
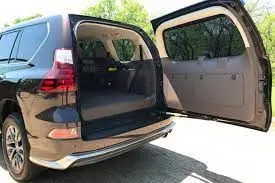
usually SUV types of the vehicle comes with side mounted Back Door.
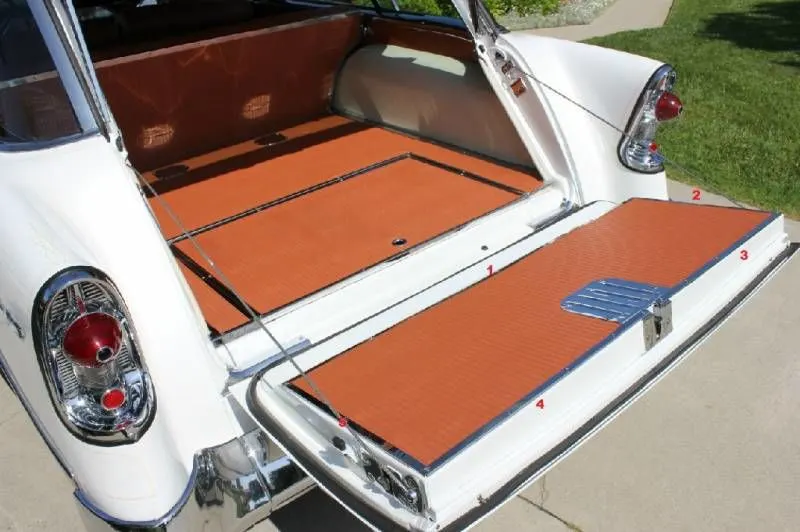
Bottom Mounted Back Door
Design Consideration for Making Back Door:-
- Functional Requirement of Hinge and gas stay.
- Rear visibility criteria.
- Luggage volume area.
- Crash Analysis.
- Bend Test, Dent Test, Torsion Test & Endurance Test.
- Rear Crash Regulation.
- Gap and flushness Requirements.
Why material Selection is a Major problem during making of back Door ?
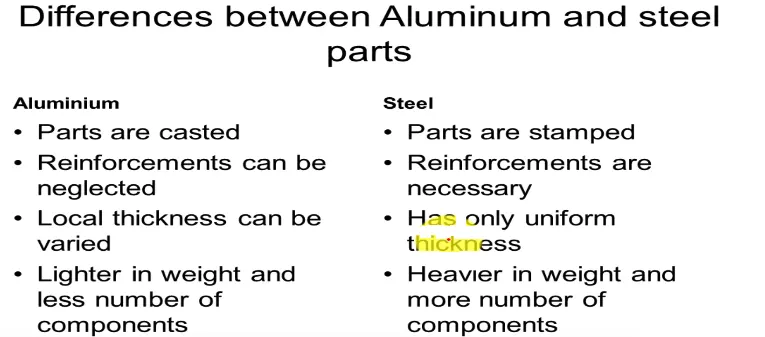
- The major problem in back door is material selection. mostly in past days steel is used, but it makes a very problems the steel parts have heavy weight,so it reduces the fuel economy, insted of steel presently in high end cars aluminium is used, the main objective of aluminium it have less desnser material and its sutaible for complex shapes, and it also gives the thcikness locally because it it done cating, in case of steel we used deep drawing operation.
- There are some of the advatanges and disadvantages are there
The components designed in this project are:-
- Back Door Outer Panel
- Back Door Inner Panel
- Hinge Reinforcement LH and RH
- Gas Stay Reinforcement LH and RH
- Wiper Motor Reinforcement
- Latch Reinforcement.
Back Door Outer Panel :-
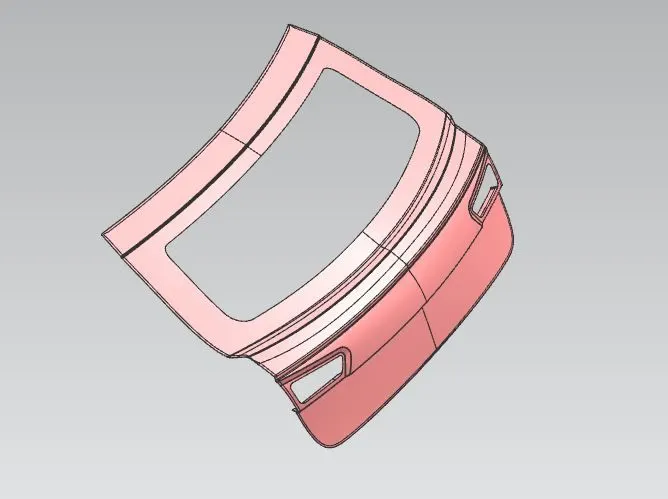
- The Outer Panel is the styling surface of the back door design.
- Other components of the backdoor are designed with reference to the outer panel surface.
- It acts as the outer cover & deals with the aesthetics of the car.
In this design outer panel is divided into two-part.
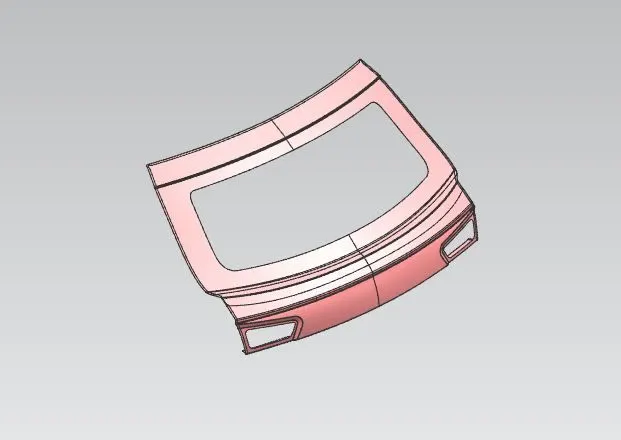
- Outer Upper Panel
- Outer Lower Pane
Outer Upper Panel :-
-
The Outer Upper Panel Extracted from a provided Classic surface.
-
The panel is modified for the required design with the surface tools of NX CAD.
-
The thickness provided to the outer panel is 0.75 mm .
-
Hemming is provided with corner reliefs.
Outer Lower Panel :-
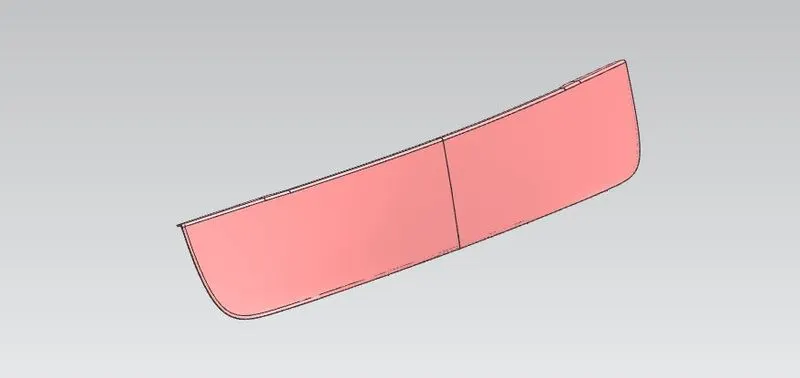
- The Outer lower Panel Extracted from the given Classic surface.
- The panel is modified for the required design with the surface tools of NX CAD.
- Here also we provided thickness to the outer lower panel is 0.75 mm .
- Hemming is provided with corner reliefs.
- After Complete all the work in Back Door Outer Upper pannel And lower Panel we Join both the component through the spot welding or Seam welding Operation.
Tooling Direction:-
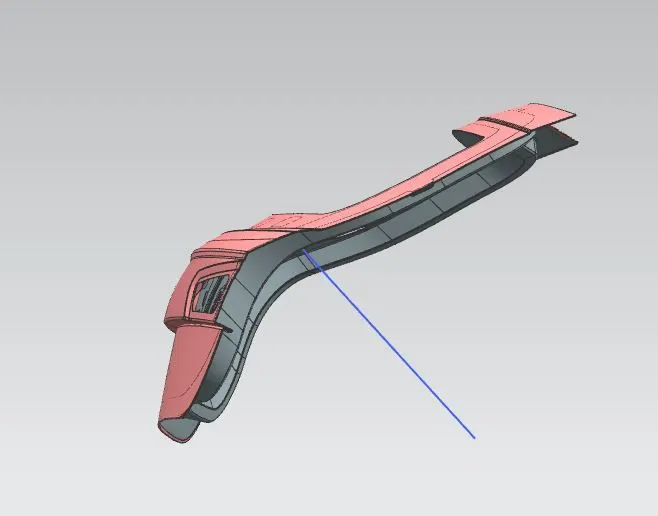
- Here the Blue Colour Line Represent the Tooling Direction.
- Before starting to design the inner panel of the back door the tooling direction for Deep Drawing purposes should be created.
- Then the styling surface needs to be checked properly and analyzed since it might have irregularities, hence it must be fixed first.
- The back door was designed using a top-down approach that means we take Reference as Outer Panel.
Back Door Inner Panel :-
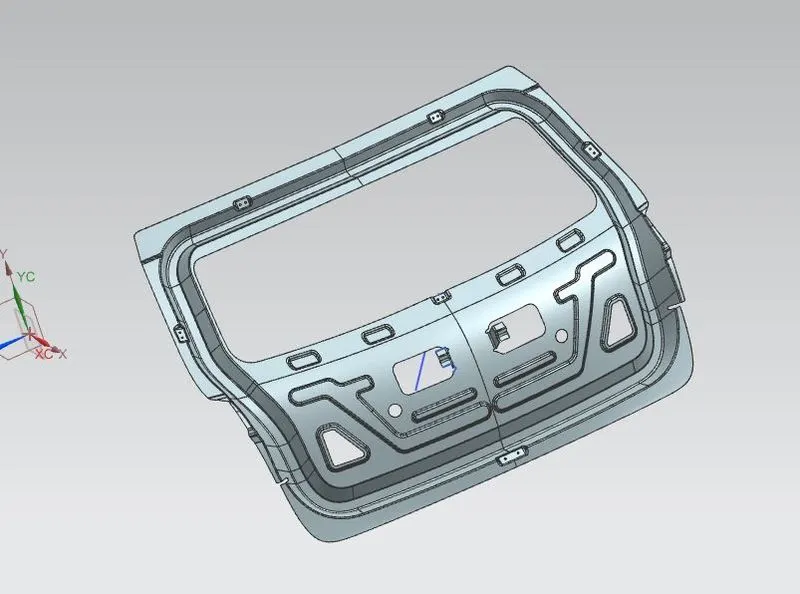
-
The Inner Panel Extracted from the Outer panel Surfaces.
-
The panel is modified for the required design criteria and dimention by using the tools of NX CAD.
-
The thickness also provided to the inner panel is 0.75 mm.
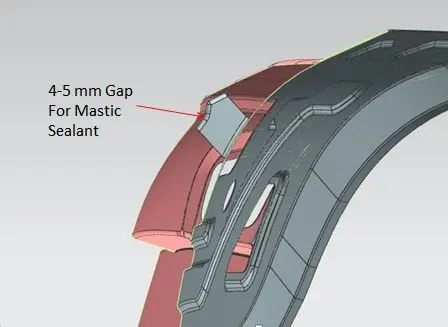
MASTIC SEALANT:
The mastic sealant is used to fix the inner panel and the outer panel which increases the NVH factor & stiffness of the back door.
HINGE, GAS STAY, WIPER MOTOR & LATCH & STRIKER EMBOSS:-
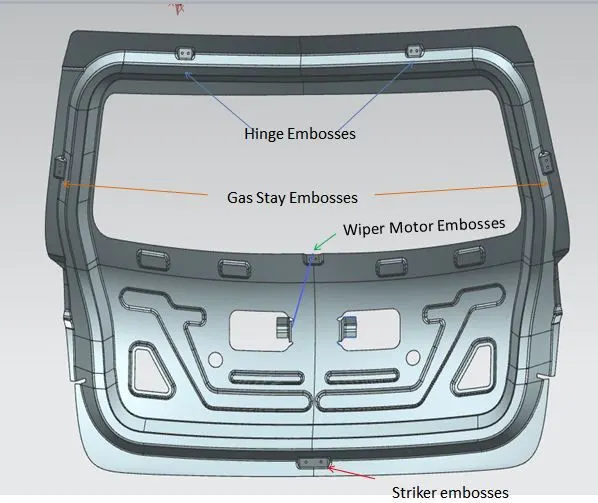
- The top Part of the Inner Panel embosses Denoted the hinge emboss which was created using the datum plane and emboss feature in NX.
- It is also designed in a way that the emboss should have a flat surface for assembling the hinges using it.
- The Drilling Holes created on the embosses is along the tooling Direction axis.
- The left and Right part of the inner panel embosses denotes the gas stay emboss which was created using the surface of the connecting flange.
- In the middle part of Inner panel emboss denotes the Wiper motor emboss which was created using the surface of the connecting flange.
- In the bottom Part Of the Inner Panel emboss denotes the Latch and Striker emboss were designed by creating a trajectory that follows the opening and closing of the back door with respect to the axis of the hinge.
TRAJECTORY :-
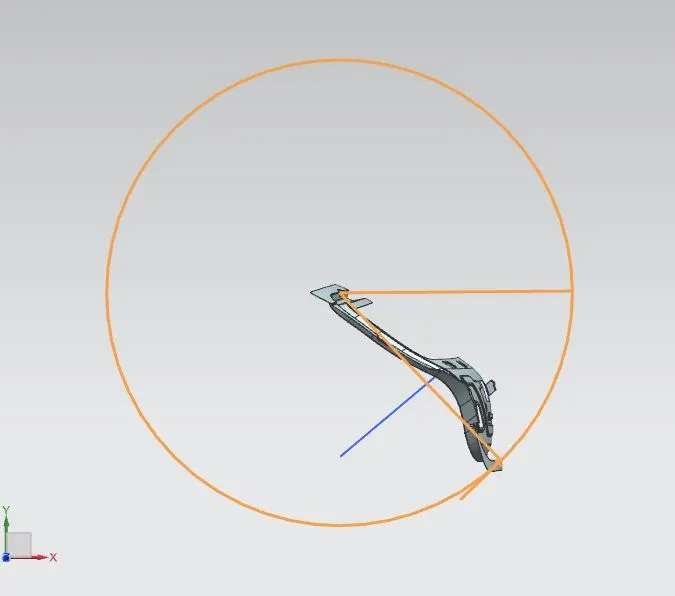
- The position of the hinge should be perpendicular to the latch at the time of latch and striker meets.
- The circle is drawn from the center of the hinge axis to find the path of the striker and perpendicular to the path
HEMMING:-
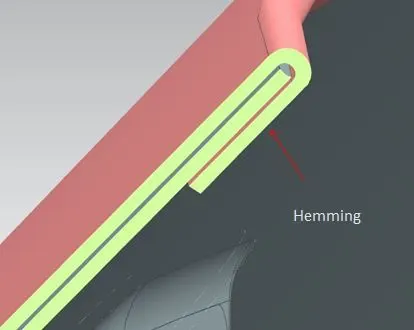
- Hemming & seaming are two similar types of metalworking processes in which a sheet metal edge is rolled over onto itself.
- Hemming is the process in which the edge is rolled flush to itself
- The outer panel was designed as two different parts named as outer upper panel and outer lower panel.
- After designing the outer panel the Hemming was created by offsetting the surface with the help of face blend & swept surface.
- The two different outer panels will be joined using Blanking
CORNER RELIEF:-
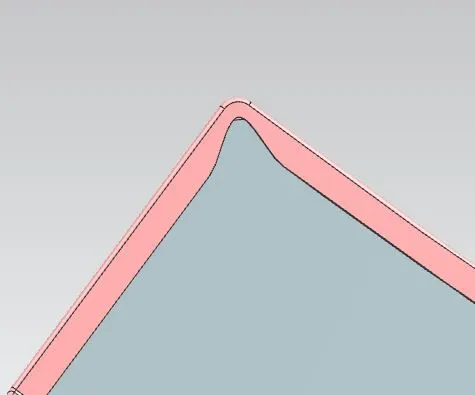
- During the hemming process, when giving the Corner Relief helps to Reduce the stress consideration and control sheet metal material behavior & to prevent unwanted deformation during unbend operations & also helps to minimize the number of passes in hemming.
DESIGNING OF THE REINFORCEMENTS PROVIDED ON THE INNER PANEL: -
The thickness provided for all reinforcements is 1.5 mm.
- Hinge Reinforcement
- Gas stay Reinforcement
- Wiper motor Reinforcement
- Latch Reinforcemnet
Hinge Reinforcement :-
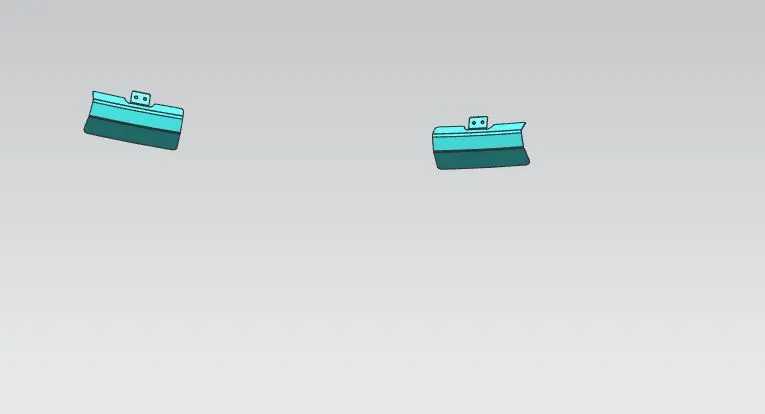
-
Hinges are allow the opening and closing of the back door.
-
One end of the hinge is fixed on the backdoor and the other end on the Roof.
-
Hinges can be placed outside or inside the backdoor.
-
The hinge reinforcements are added to compensate for the weak region due to the acting load over it and provide a good strength on that region.
Gas Stay Reinforcement :-
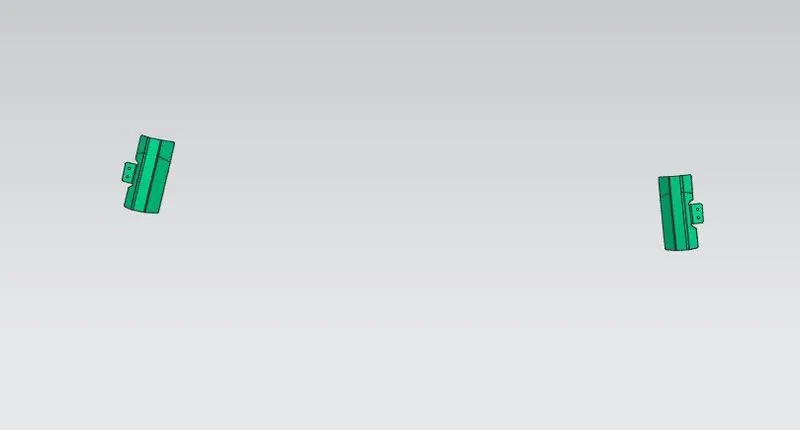
-
Gas Stay is a device used to support the back door in its open position.
-
Gas stay requires no manpower & it is engaged into support position automatically as the back door opens.
-
One end of the Gas Stay is fixed on the backdoor & another end is on the Body Side or on the Back door stationary area.
-
Embossing is provided at the Gas Stay mounting area to compensate for weakness & improve strength.
- When it used it lift the load of Back Door so that we provided the Reinforcement on that Region.
Wiper Motor Reinforcement :-
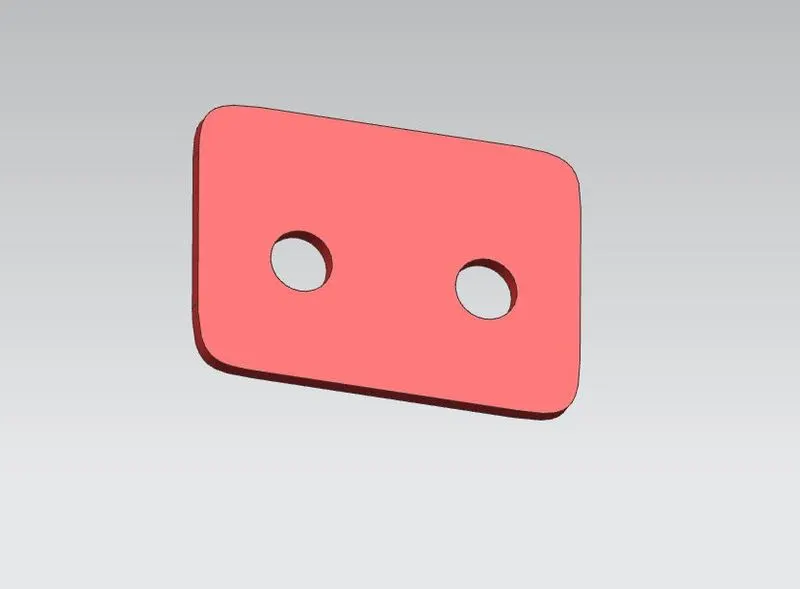
- Wiper motor reinforcement is made to mount the wiper motor assembly.
Latch and Striker Reinforcement :-
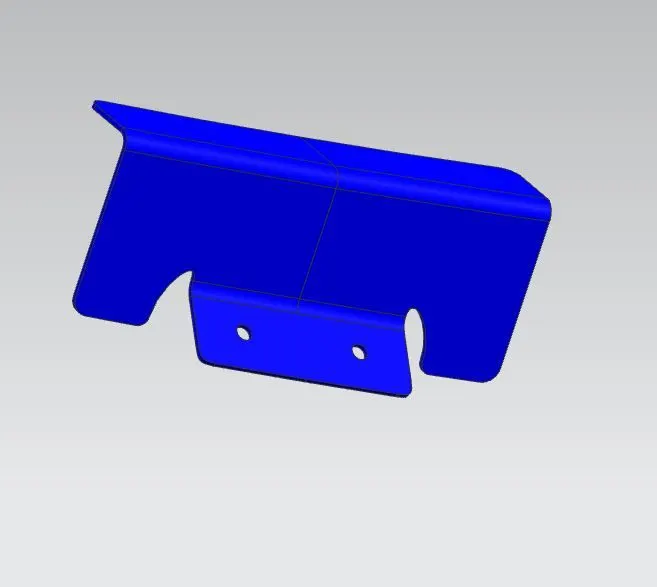
- The Latch & Striker together form the locking mechanism of the backdoor with the car.
- Due to regular opening, closing, and over slamming of the backdoor, there is stress developed in the Latch & Striker area.
- To improve the strength on that region we provided reinforcements in this area.
Gas Stay Mechanism :-
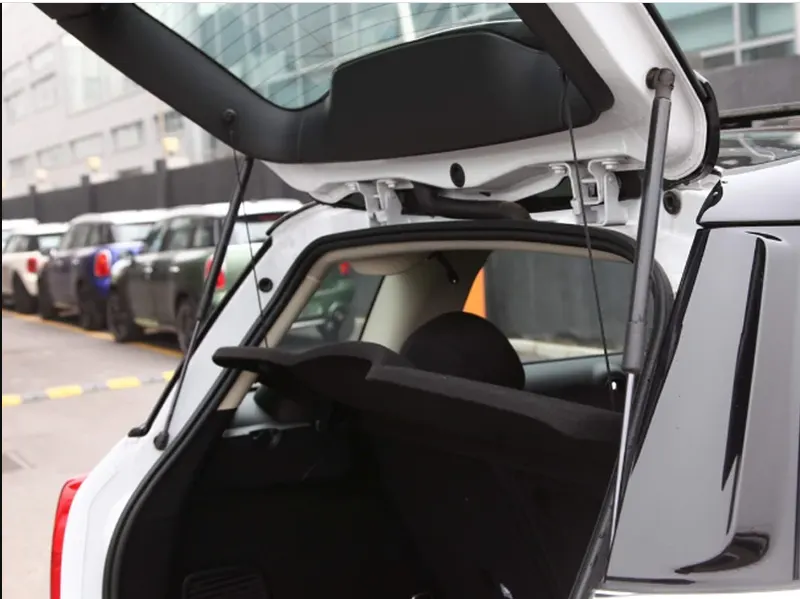
- The main purpose of these mechanisims is to open the back door without heavy efforts, because the backdoor have different parts and the weight of the back door is high, so we are not able to open the back door manually, so we introduced these two types comodities. and these also decides the premium of the car, mostly the electrically operated used in premium cars.
DRAFT ANALYSIS :-
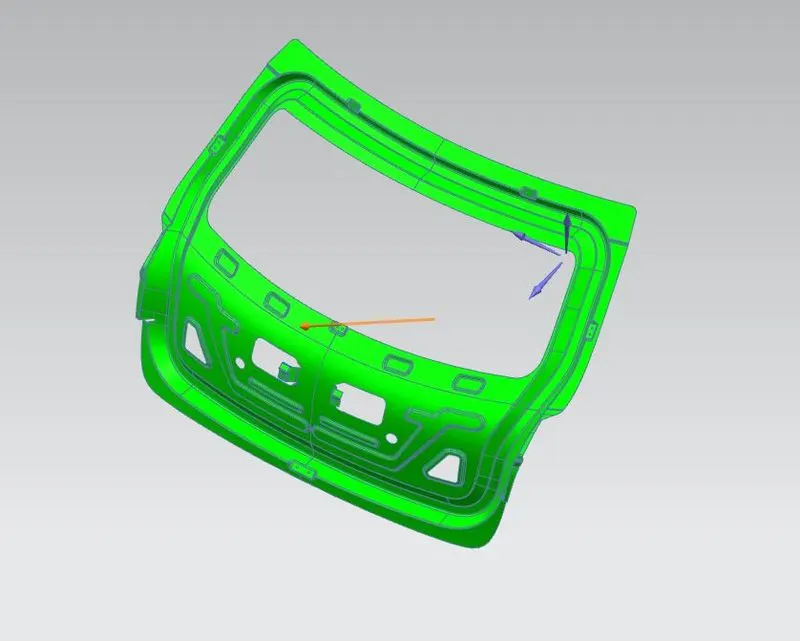
- The draft analysis was performed for the tooling direction created at first and checked that the model is suitable for manufacturing.
- Then to get a complete green portion the required changes to the draft angle of the embosses were carried out by optimizing the model.
- The Draft Analysis command is used to detect that the part drafted will be easily removed or not.
- This type of draft analysis is performed based on color ranges.
- The identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
THE MANUFACTURING PROCESS USED IN TO MAKE BACK DOOR:-
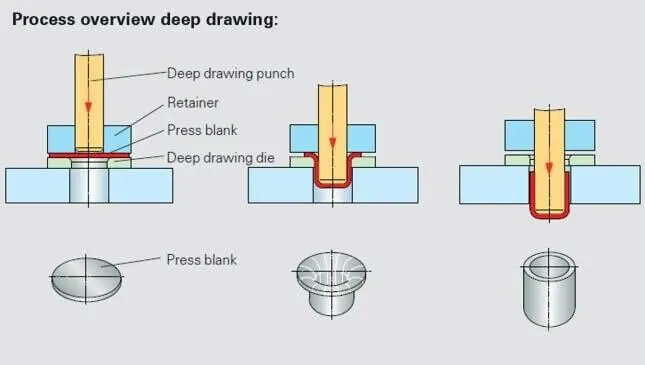
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
- First- stage drawing: The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
- Redrawing: The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
Hemming :-
- The inner & outer panels are joined by the process of hemming.
- Hemming is a forming operation in which the edges of the sheet are folded over other parts in order to achieve a tight fit. Usually, hemming operations are used to connect parts together, to improve the appearance of a part, and to reinforce part edges.
- In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming & flanging operations to join two sheet metal parts together.
- The accuracy of the hemming operation is very important since it affects the appearance of the surface & surface quality. Material deformations, which occur while the hemming process, can lead to dimensional variations & other defects in parts.
- Typical hemming defects are splits and wrinkles in the flange, material overlaps in the corner areas.
There are different types of hemming operations:-
- Conventional die hemming
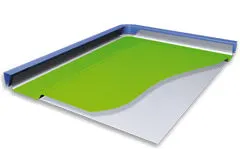
In conventional die hemming, the flange is folded over the total length with a hemming tool.
- Roll Hemming
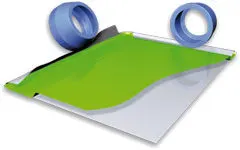
In roll hemming, the hemming roller is guided by an industrial robot to make the flange.
Blanking:-
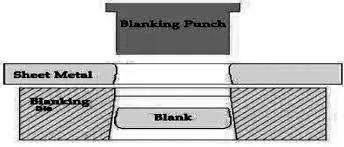
- Blanking is a cutting operation of a flat metal sheet and the sheet metal part punched out is known as blank.
- Blank is the required product of the operation and the metal left behind is considered as a waste.
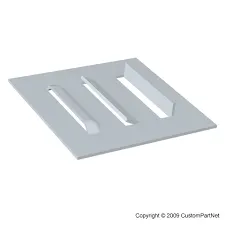
Lancing :-
- In the Lancing Process we create a Partial cut in the sheet Metal so that there is no metarial removed from the sheet .
- The left material is attached to be bent and from a shape such as vent,tab,louver.
General Analysis Of Load Cases In The Back Door :-
Bend Test:-
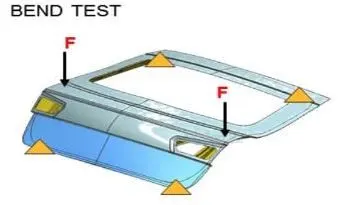
- In this test we give constraint at the corners part of Back Door and apply nominal downward force in the midle part of the back back door to observe how it comes back into their original position.
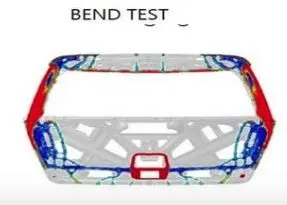
This is how the force is distributed when we apply force on it.
Torsion Test :-
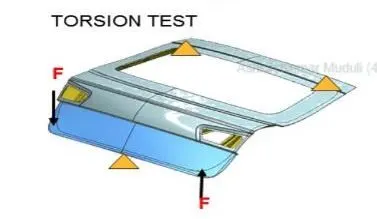
- In this test we give constraint at the two hinge part and the striker area of the back door then apply two reverse force at the bottom corner of back door and see how it behaves and how quickly it comes back into their original state.
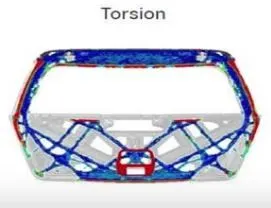
This is how the force is distributed when we apply force on it.
Abuse cases :-
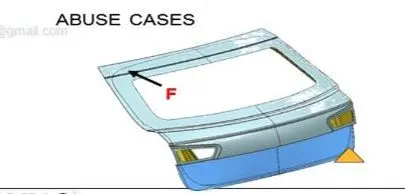
- It is the case of over slaming or hanging with door when door is opend and closed.
Assembly Load Test :-
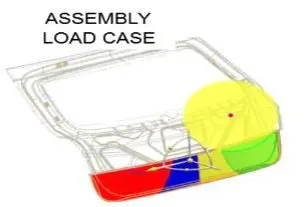
- It is the case when we assembly the body to check how much force given to the body and the door wheather stand or not.
Conclusion :-
- The back door outer and inner panel were designed with the help of the styling surface along the tooling direction and the Draft analysis was performed on the inner panel and All the reinforcements were designed and placed at appropriate positions.