Design of backdoor
DESIGN OF BACKDOOR (TAILGATE)
Objective
- To design the Backdoor/Tailgate of a Hatchback car with the A-surface provided using the proper design methodologies
- Design the Tailgate inner panel with the Hinge, Gas Stay, Wiper Motor and Latch & Striker mountings and their reinforcements
- The Inner Panel design should be manufactural by Deep Drawing process in the Tooling direction.
Introduction
A Backdoor or Tailgate is the door at the rare most end of the car which encloses the boot space. It also has the Wiper Motor mounted on it, along the Tail Lamp, Gas Stay and Latch & Striker.
The Backdoor is designed to be able to accommodate the various components mounted on it and also affects the rear visibility and boot space.
The material used to manufacture a Backdoor varies according to the budget of the project and can be made of Plastic, Steel or Aluminum.
Typical Parts of a Backdoor
- Outer panel (upper & lower)
- Inner panel
- Hinge reinforcement (LH & RH)
- Gas Stay/ Power Lifter reinforcement (LH & RH)
- Wiper mounting reinforcements
- Latch & Striker mounting reinforcements
Design Criteria of a Backdoor
- Rear Visibility Criteria or Regulations
- Boot Space
- Rear Crash Regulation and Requirements
- Joining techniques followed such as Hemming, Spot Welding etc.
- Manufacturing technique used to create it
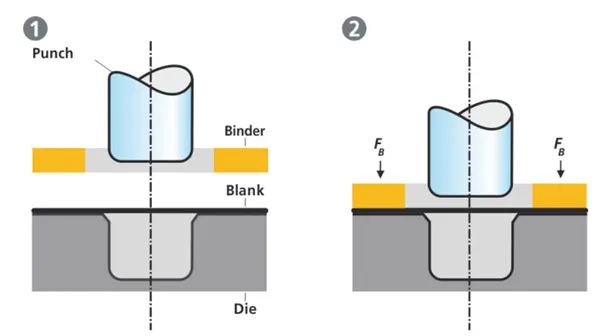
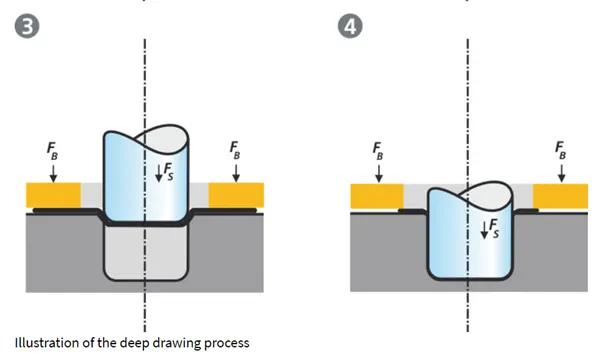
Deep Drawing process
Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered "deep" drawing when the depth of the drawn part exceeds its diameter. This is achieved by redrawing the part through a series of dies. The flange region (sheet metal in the die shoulder area) experiences a radial drawing stress and a tangential compressive stress due to the material retention property. These compressive stresses (hoop stresses) result in flange wrinkles (wrinkles of the first order). Wrinkles can be prevented by using a blank holder, the function of which is to facilitate controlled material flow into the die radius.
In the automotive industry, deep drawing is usually carried out using rigid tools.
Hemming
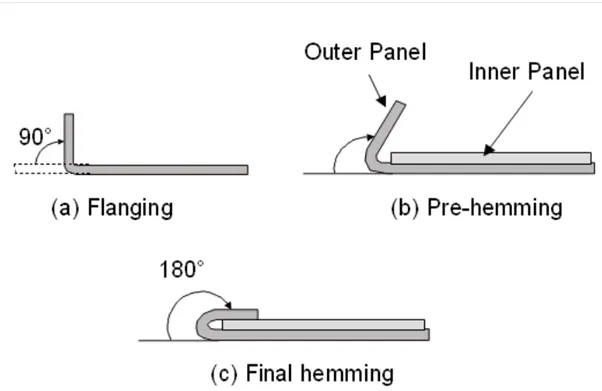
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas or material roll-in. This is why it is important to use simulation tools in order to, on the one hand, better understand the hemming process and, on the other hand, significantly reduce the number of “trial and error” loops during tryout und production.
There are various types of hemming operations:
- Conventional die hemming
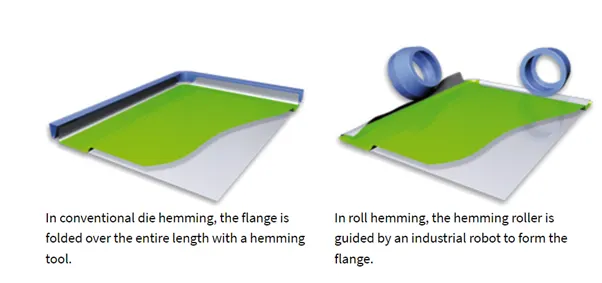
Conventional die hemming is suitable for mass production. In die hemming, the flange is folded over the entire length with a hemming tool. Normally the actual hemming is a result of a forming operation in which the flange is formed with a hemming tool after the drawing and trimming operations have been completed. The formed flange is then hemmed in several process steps. These steps include, for example, the pre-hemming and final hemming depending on the respective opening angle of the flange. Production plants for conventional die hemming are very expensive, but the cycle times are very low.
- Roll hemming
Roll hemming is carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller which follows a defined path.
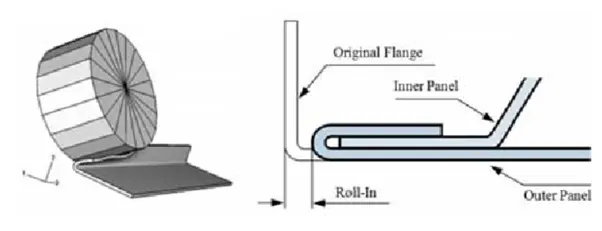
3 steps of roller hemming process
Uses of Hem
Hems are commonly used to re-enforce, hide imperfections and provide a generally safer edge to handle. When a design calls for a safe, even edge the added cost of material and processing of a hem is often preferable to other edge treating processes. Designers should look beyond a single small flat hem to treat edges. Doubling a hem can create an edge perfectly safe to be handled without almost regard for the initial edge quality. Adding a hem in the ‘middle’ of a bend profile can open the doors to a variety of profiles not possible without fasteners or welding. Even without sophisticated seaming machines a combination of two hems can create strong, tight joints with little or minimal fastening. Hems can even be used to strategically double the thickness of metal in areas of a part which may require extra support.
DESIGN OF THE PARTS
1. Outer Panel (Upper & Lower)
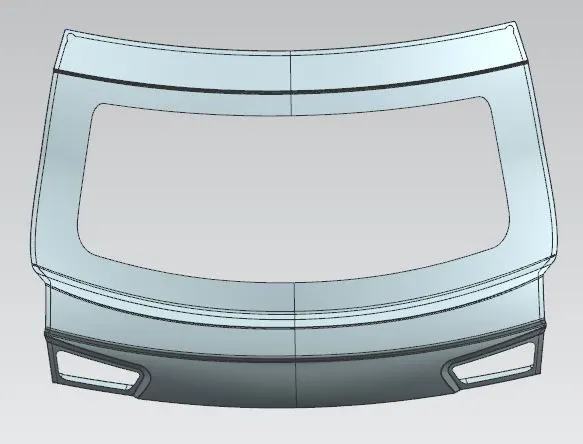
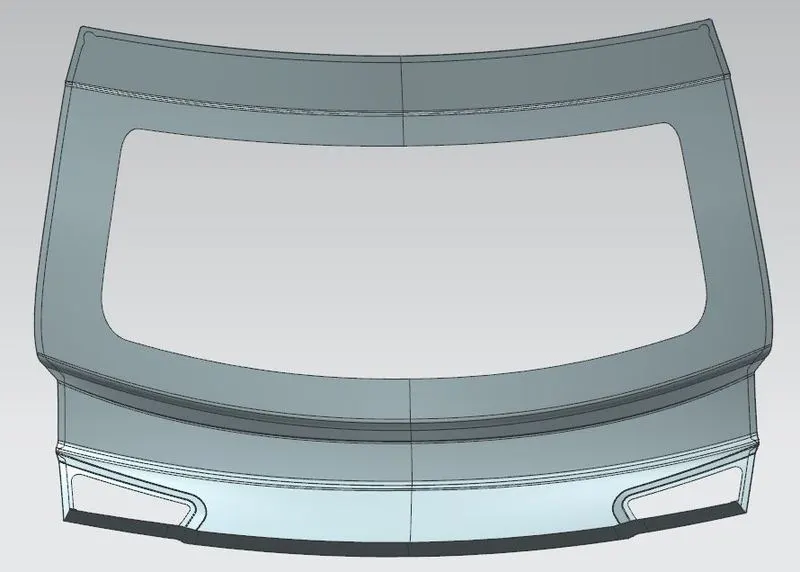
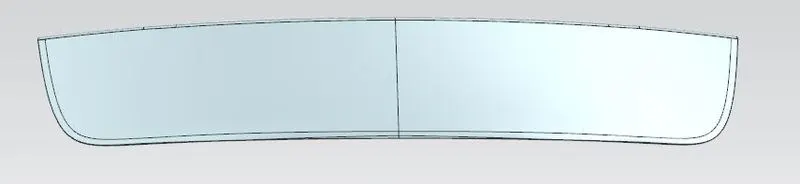
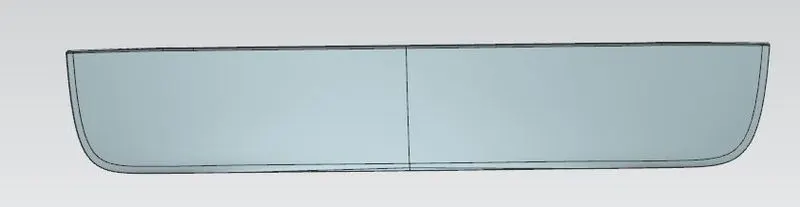
- The upper and lower panels of the outer panel is made out of the styling surface provided and given a thickness of 0.75.
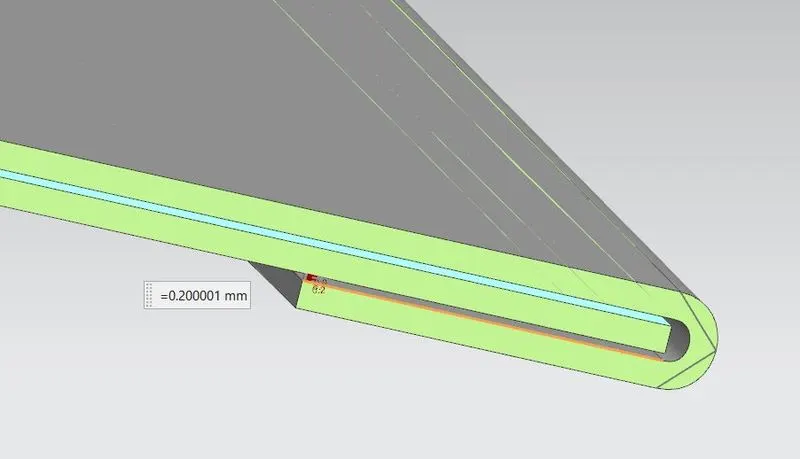
- Hemming is created in these panels by offsetting the surface according to the panel thickness and clearance required between the outer and inner panel for hemming.
- Excess material is removed from the lower surface and the two surfaces are joined by means of Swept surfaces which created the hemming.
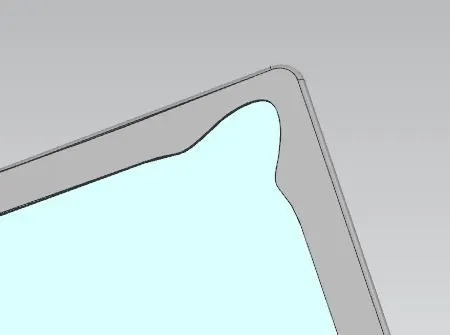
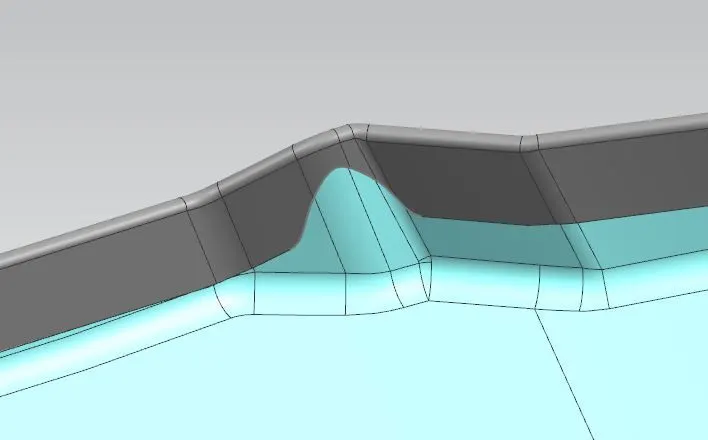
- Corner reliefs are also provided to prevent deformation during hemming process.
Upper Panel
Corer Reliefs
Lower Panel
Hemming
2. Inner Panel
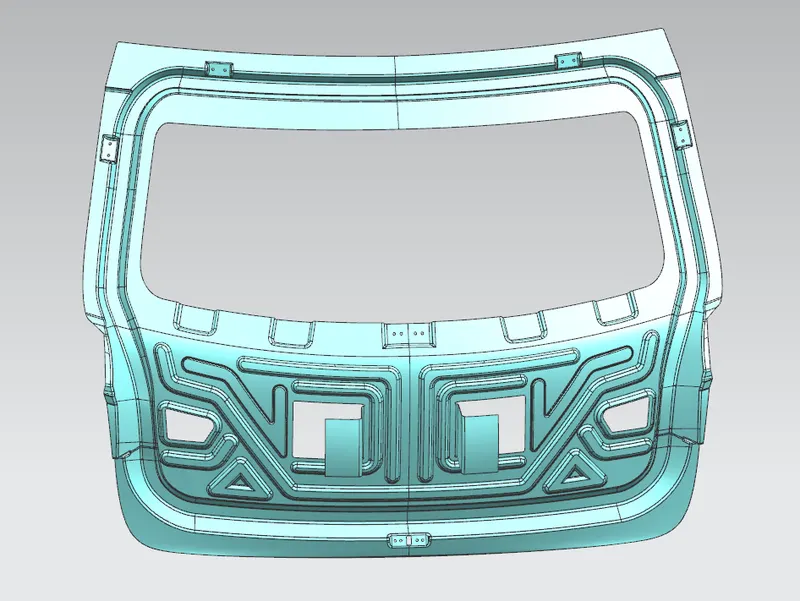
The inner panel is also created from the styling surface provided and the below steps are followed to design it.
- The tooling direction for the deep drawing process is created first since the design of the inner panel is made with respect to the tooling direction
- An effective sealing flange is created and the inner panel shape is designed along with it
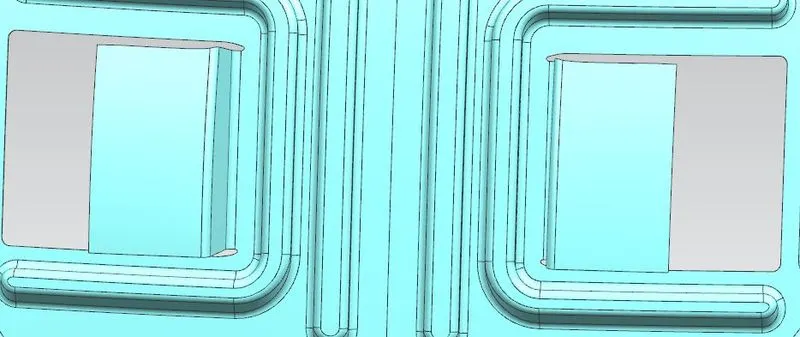
- A flange is created for Mastics, the flange attaches the inner and outer panel by means of mastics and thus it is at a 5mm distance from the outer panel.
- A hole is also provided for the tail lap wiring and harness
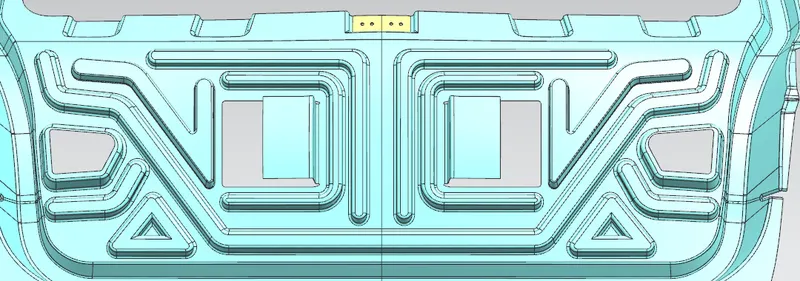
- Embosses in the shape of ‘V’ or ‘Y’ is created, the shape of the embosses help dissipate the force which would be applied to the Tailgate in case of a collision
- The Hinge, Gas stay, Wiper and Latch & Striker mountings are created, wherein the Latch & Striker.
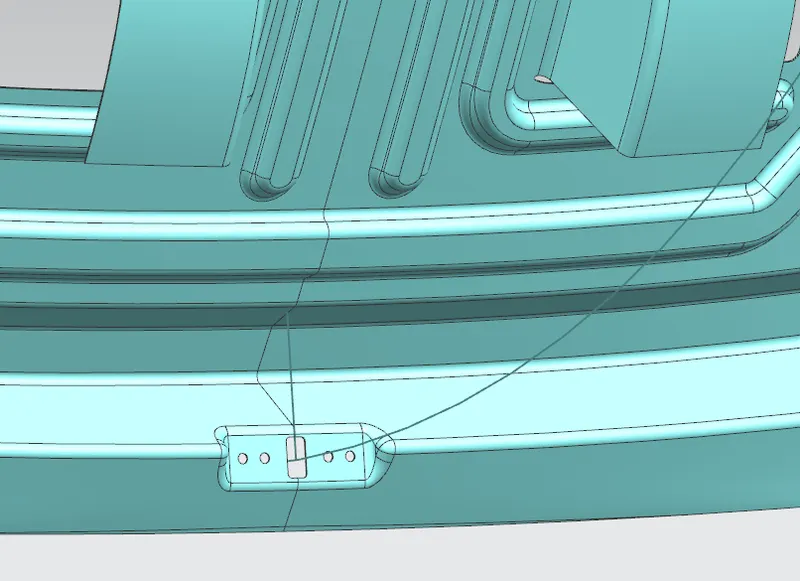
- For the Latch & Striker mounting position a Backdoor trajectory is created from the hinge axis, this shows the path followed by the backdoor when opening or closing. The mounting of the latch has to be perpendicular to this hinge axis for the backdoor to open and close properly.
- The Inner panel is also provided with a thickness of 0.75
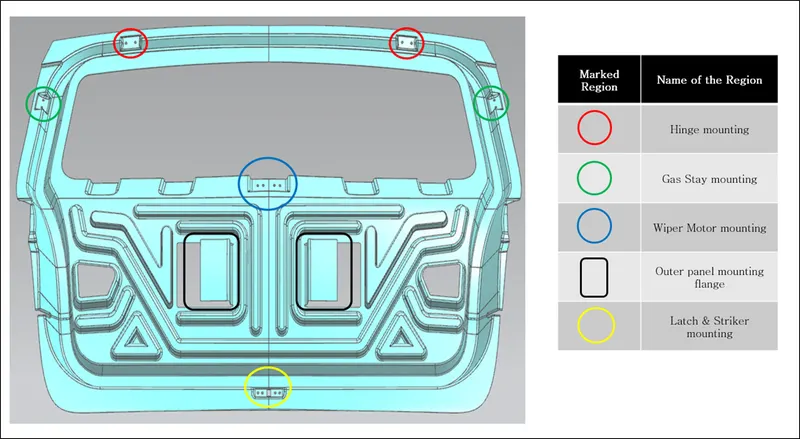
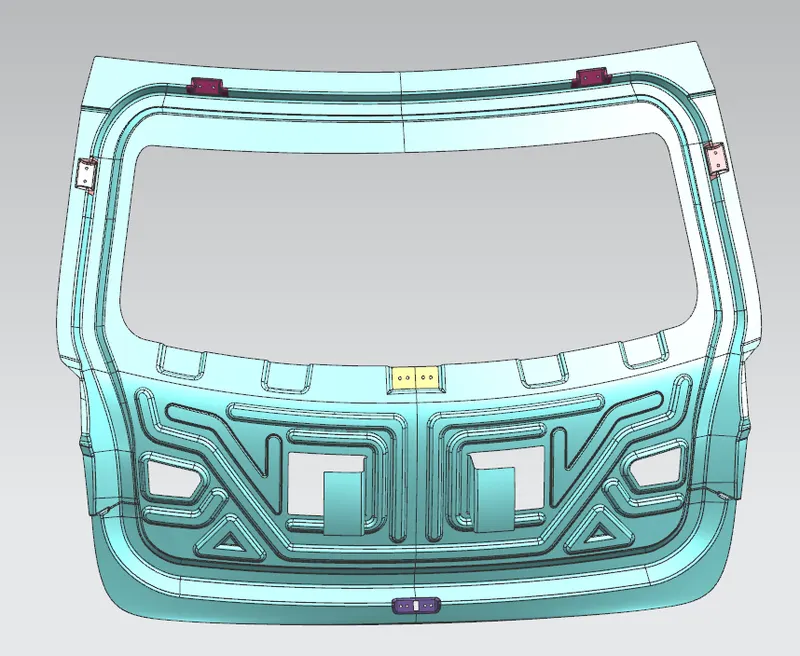
Outer panel mounting flange (position for mastic)
Embosses
Hinge mounting position
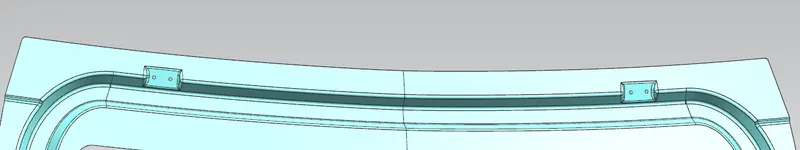
Gas Stay mounting position
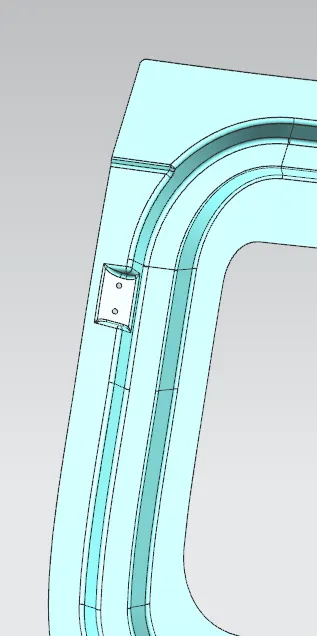
Wiper Motor mounting position
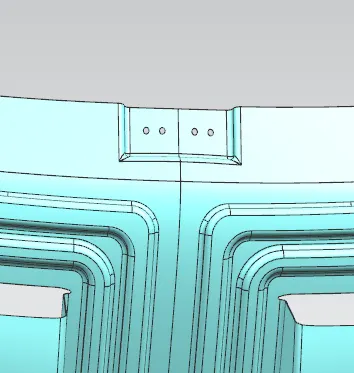
Hood Trajectory and Latch & Striker Mounting position
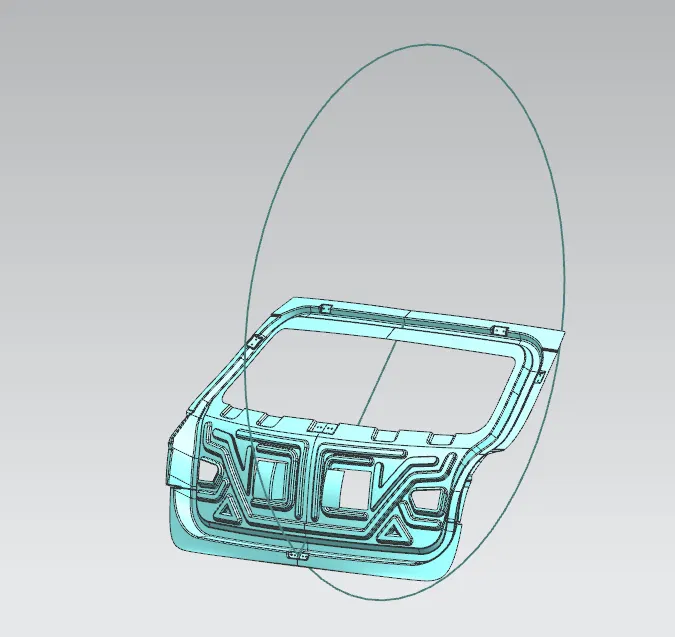
3. Reinforcements
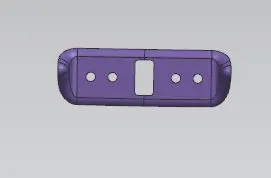
- Reinforcements for the Hinge, Gas Stay, Wiper and Latch & Striker mounting are created since these parts of the Inner panel would be subjected to load thus making the areas susceptible to damage. Reinforcements are added to compensate for the weak regions.
- These are created by extracting the inner panel geometry and cutting out the required portion from it for the reinforcements.
- The thickness provided for each reinforcement is 1.5mm
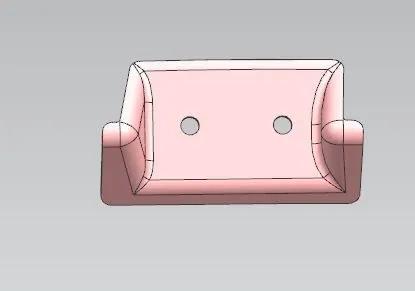
Hinge Reinforcement
Gas Stay Reinforcement
Wiper Motor Reinforcement
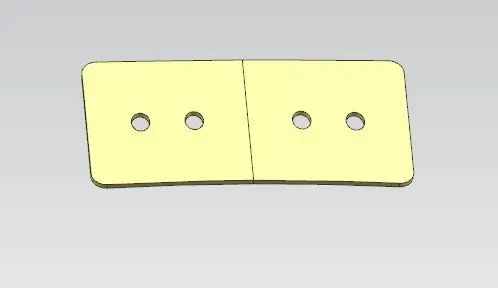
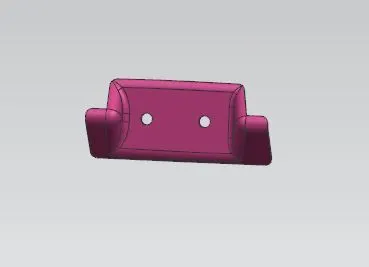
Latch & Striker Reinforcement
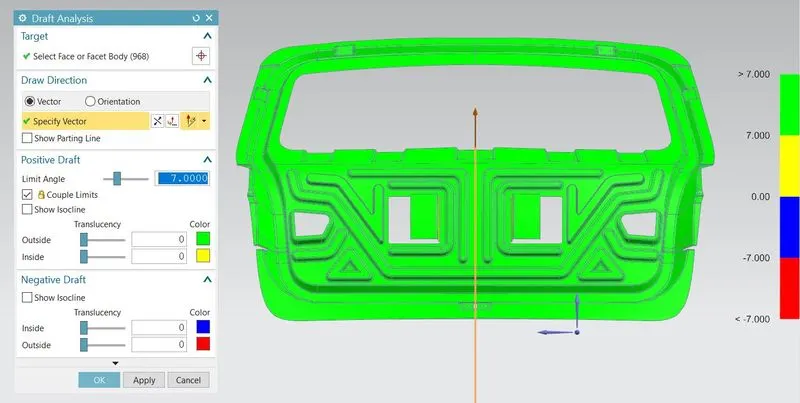
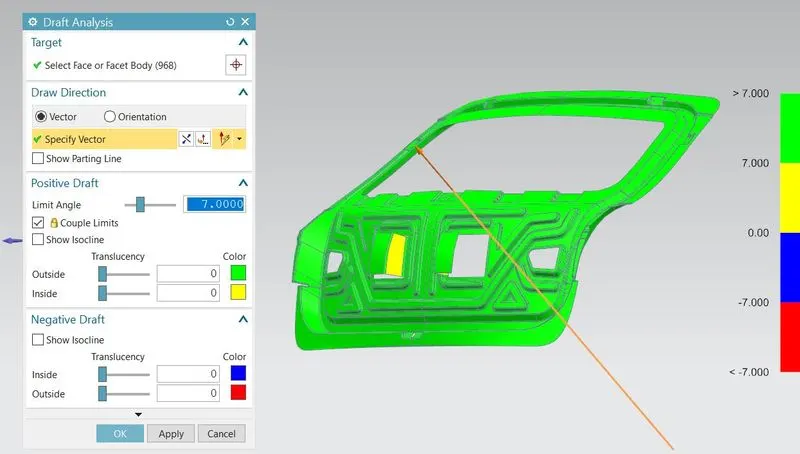
DRAFT ANALYSIS
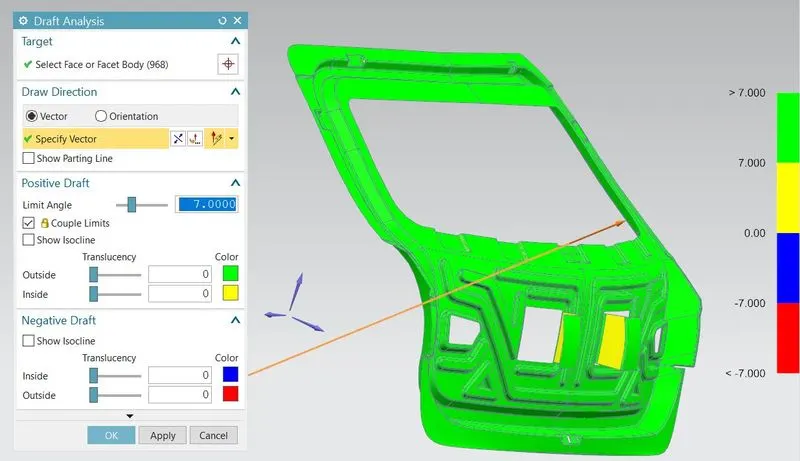
Draft analysis is done to check if the designed inner panel can be deep drawn in the tooling direction created, at a positive draft angle of 7°.
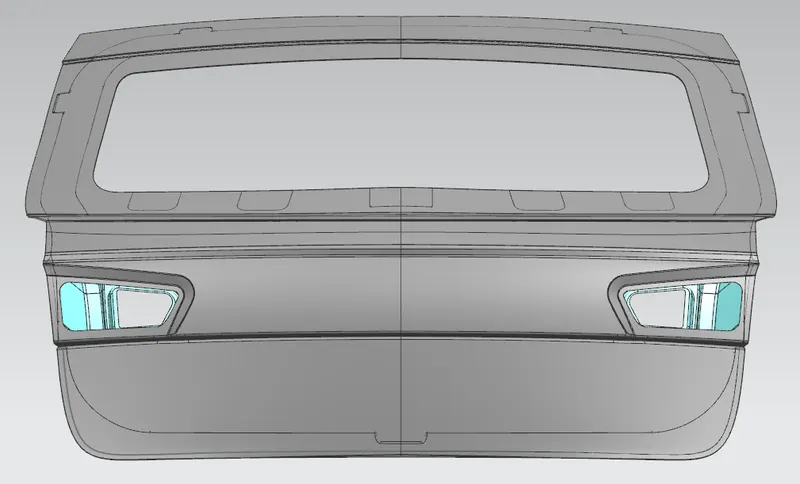
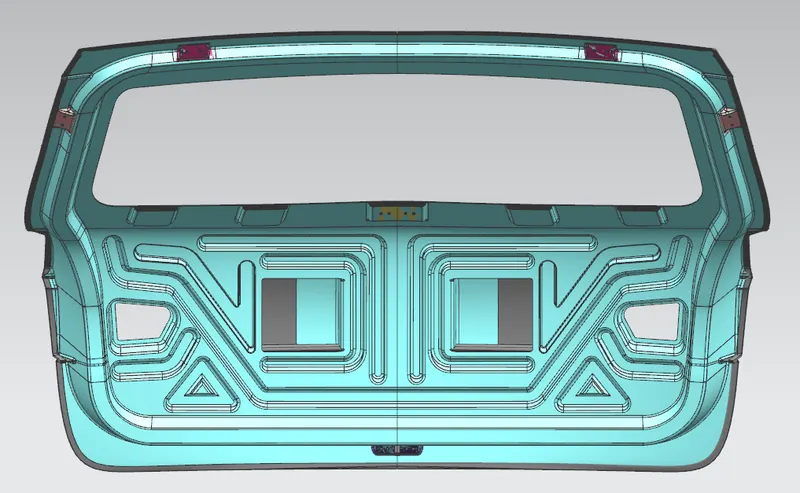
VIEWS
CONCLUSION
The Backdoor was created successfully with the required mountings and reinforcements and the design cleared the draft analysis thus making it manufactural by deep drawing process