Week 9 - Project 1 - Door Applique Design with Engineering Features
Door Applique design with engineering features
Introduction
3-2-1 location principle
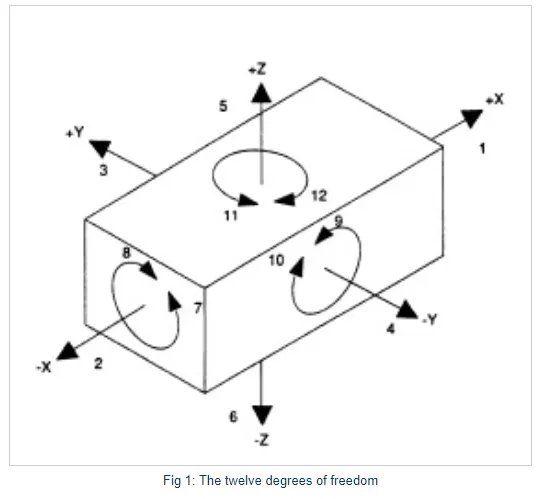
Any 3 dimensional object in space has 12 degrees of freedom along the 3 axes
- Translational position along the X-axis
- Translational position along the Y-axis
- Translational position along the Z-axis
- Rotational position about the X-axis
- Rotational position about the Y-axis
- Rotational position about the Z-axis
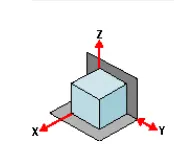
3-2-1 principle entails three steps that employ three, then two, then one fixed points of known location. Since that adds up to six fixed points, it’s also known as the six point method.
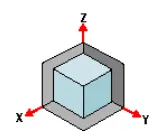
In the three steps of the 3-2-1 method, three mutually perpendicular planes, called datum planes, are introduced, one at each step. These three planes define the workpiece position, and together with opposing clamping forces fully constrain the part.
First Plane
Geometry tells us that three points are required to define a plane. This is the "3" in 3-2-1. So, three specific points are used to define the first plane. The part’s six degrees of freedom have now been reduced to three. It can still move along the X or Y axes, and it can still be rotated about the Z axis. (The part cannot move along the Z axis because it is held against the plane by clamping force).
Second Plane
A second plane, if it is perpendicular to the first, can be defined by two points, the "2" in 3-2-1. The part is now constrained to one degree of freedom: movement along the Y axis. (The part cannot move along the X or Z axes because it is held against the planes by clamping force.)
Third Plane
A third plane, if it is perpendicular to both of the first two planes, can be defined by one point, the "1" in 3-2-1. The part is now entirely constrained. It cannot move along or rotate about the X, Y, or Z axes. (Remember that the part is held against each of the three planes by clamping force.)
4 way and 2 way locators
4 way locators restricts 4 degrees of freedom along 2 axes, and a 2 way locator restricts 2 degrees of freedom along 1 aixs
Heat Staking
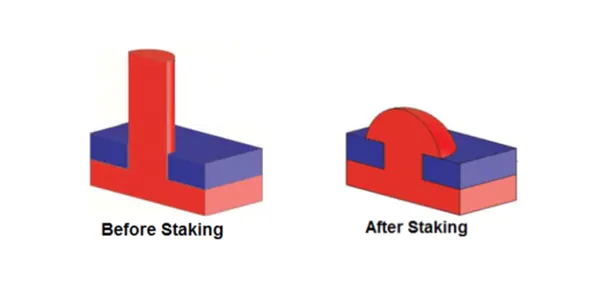
Heat staking technology is quite simple in concept. Whenever two or more components need to be attached to one another, and at least one is made of a thermoplastic, a combination of heat and pressure can be used to reform the plastic to the many shapes or profiles to retain or join the parts together.
This creates a solid, hardware-free bond that uses the plastic’s inherent strength to keep the finished assembly together.
The main advantage to heat staking, when compared to fastener-based technologies, is that manufacturers can perform all heat staking in one machine cycle and motion versus individual motions required for each fastener. A secondary benefit is that the manufacturers do not need to change the base material – it can remain “AS-IS” while the plastic is heat staked to conform to its final dimensions.
Process
Design of the Door applique
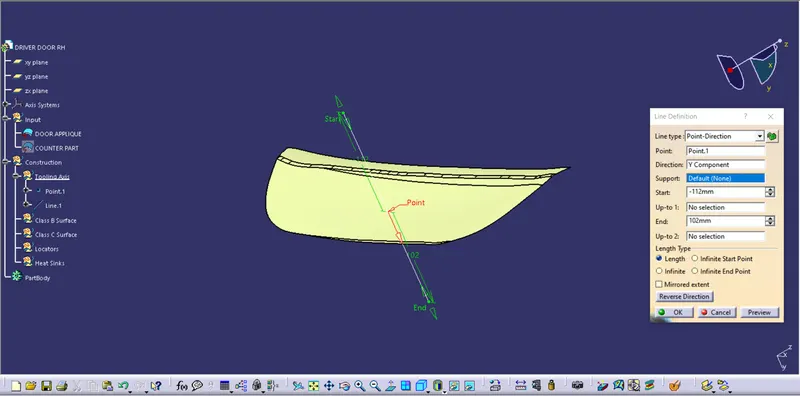
- The tooling axis is created on the midpoint of the A surface in the Y axis
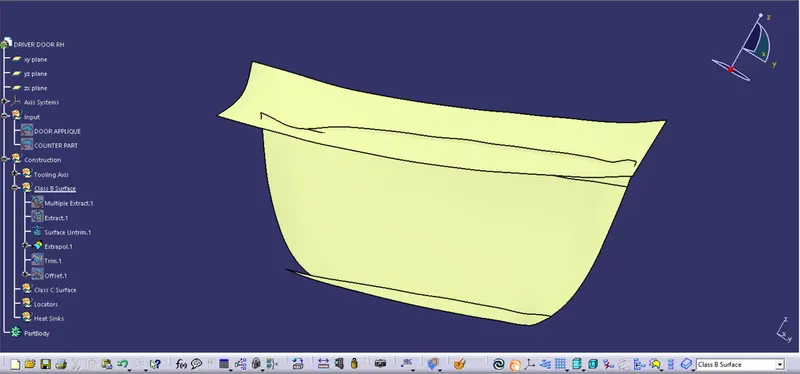
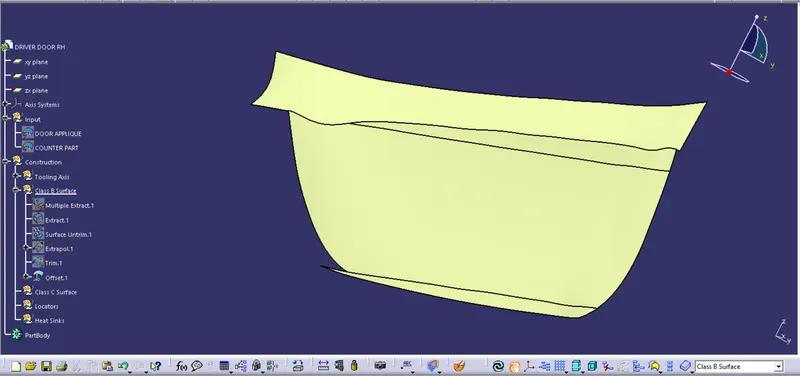
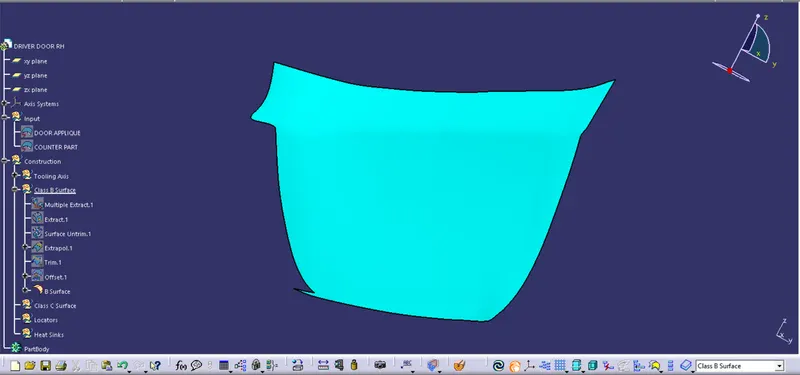
- The B surface is created by extracting the individual faces from A surface, extrapolating them and trimming them with each other and offsetting the trimmed surface by 2.5mm
- The fillets are applied on the offset surface and this is the B surface of the Door applique
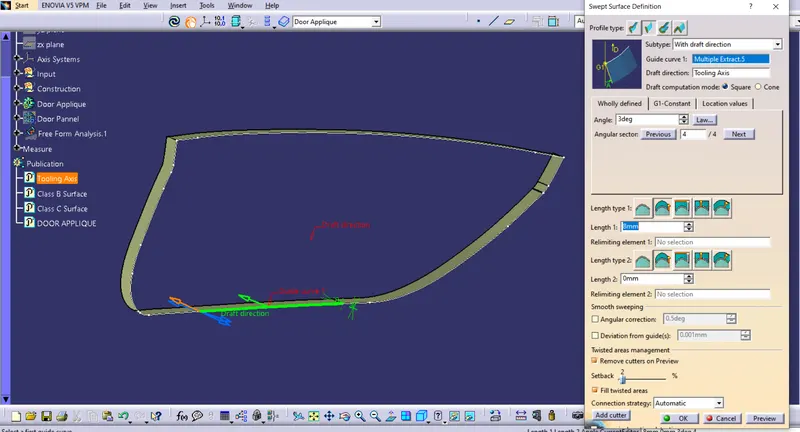
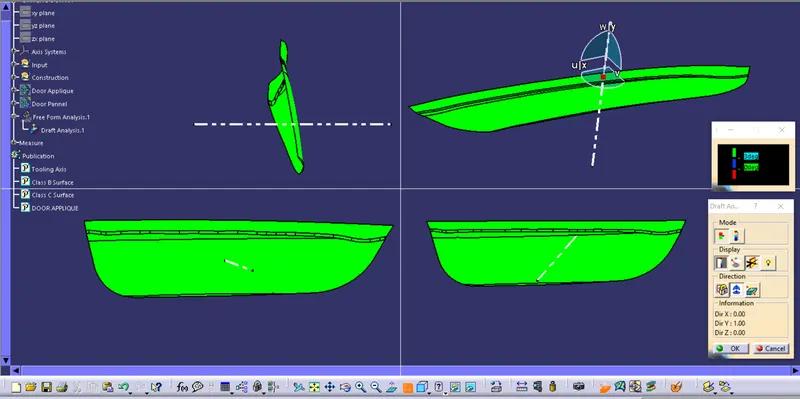
- The C surface is created by extracting the boundary of the A surface and sweeping them along the tooling axis with a draft angle of 0.5°
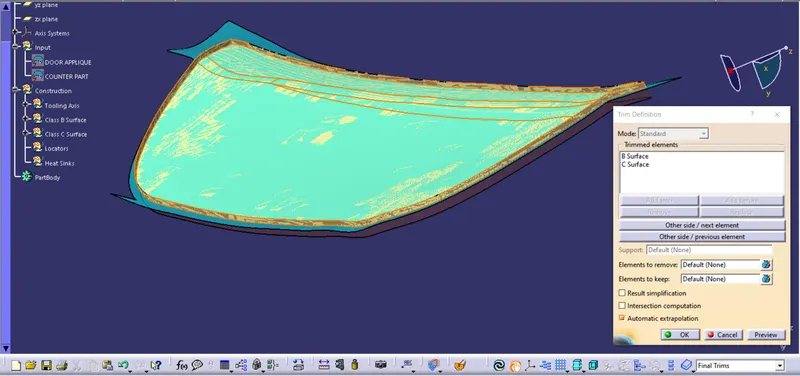
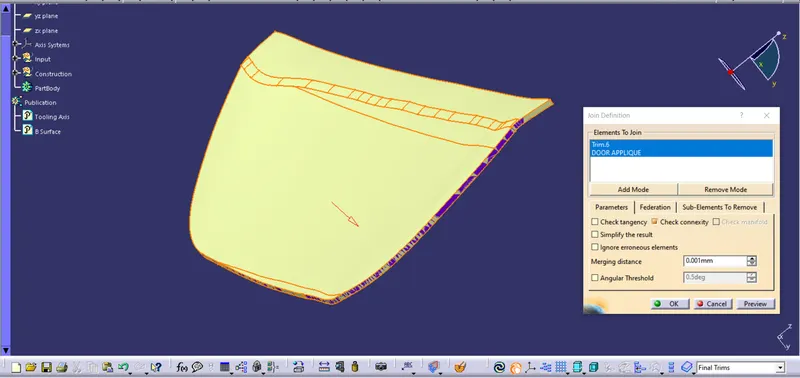
- The B surface is trimmed with the C surface and then it is joined with the A surface to create a closed surface body
- The closed surface is then converted to a plastic body
Tooling axis
B surface
C surface
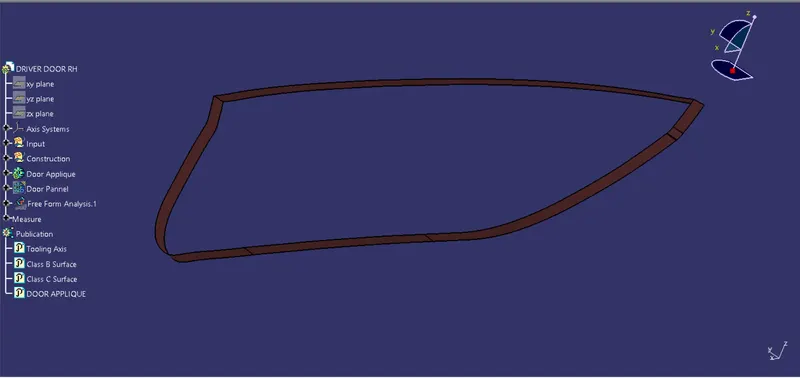
Final closed surface body
C and B surface trim
Joining of the surfaces
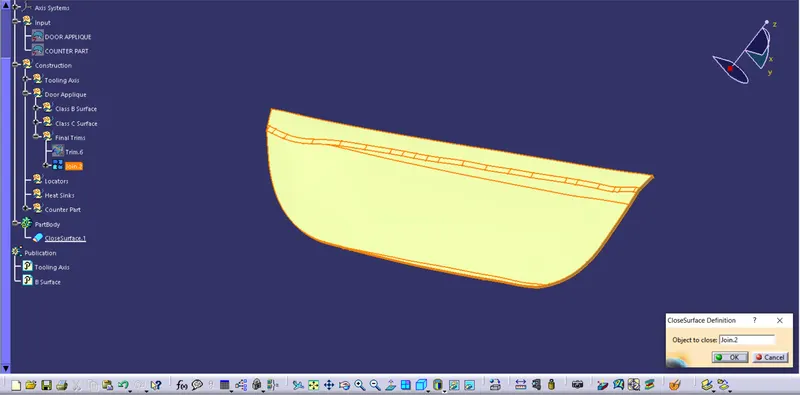
Final Plastic body
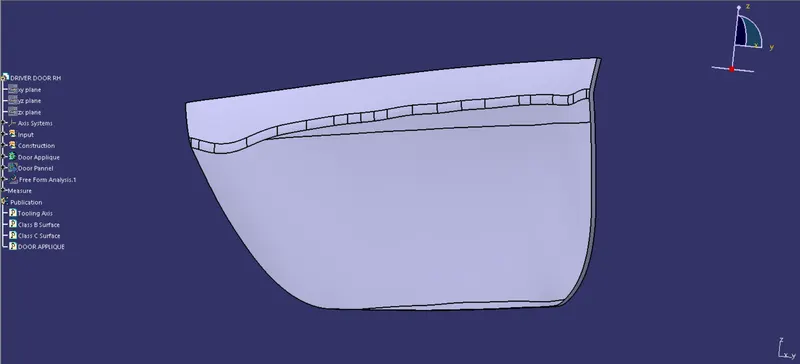
Design of 4 way and 2 way locators and Heat stakes
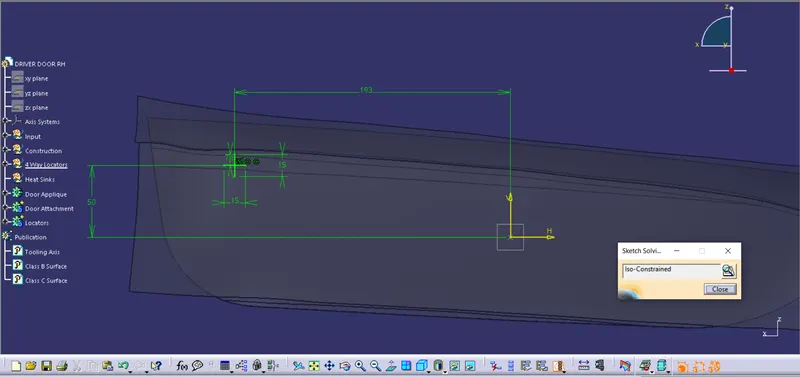
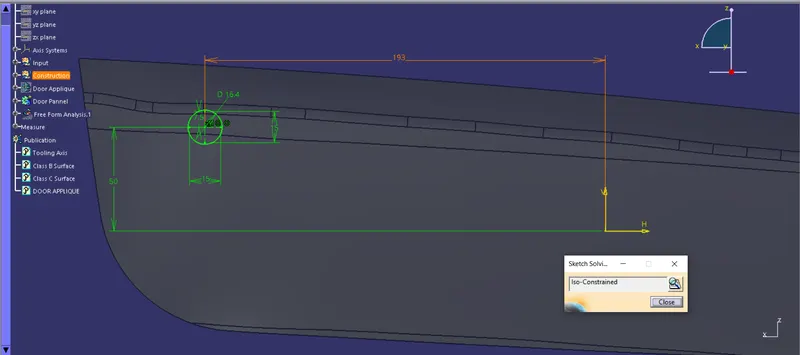
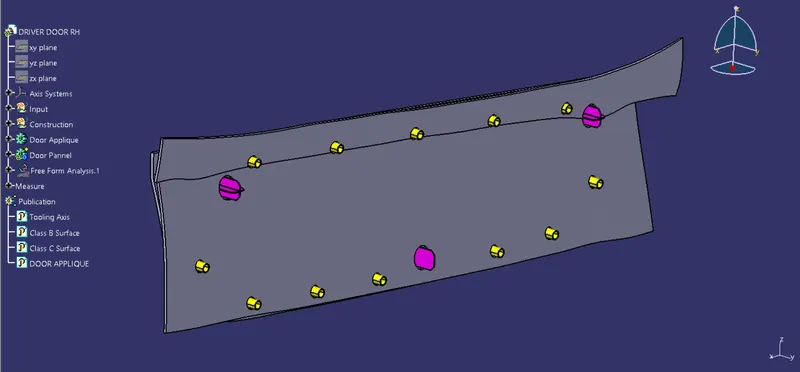
- Two 4 way locators are designed and positioned at the two extreme corners of the Door applique.
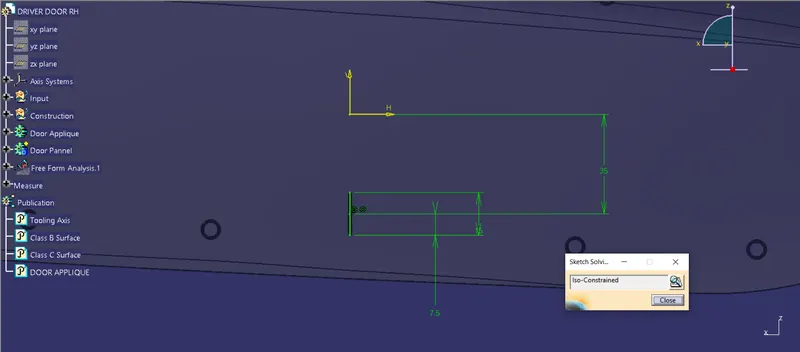
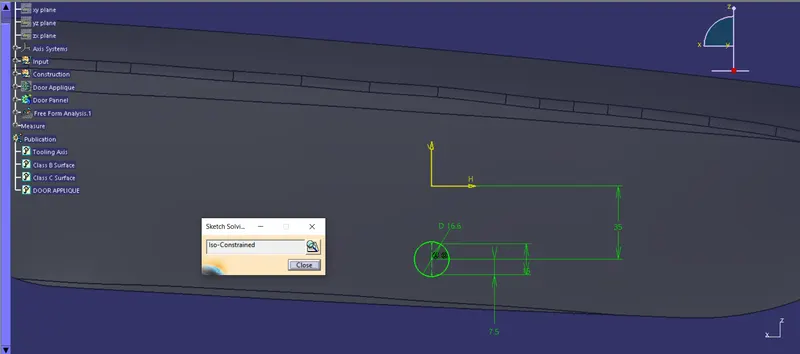
- A 2 way locator is then created at the middle of the door applique at the bottom end
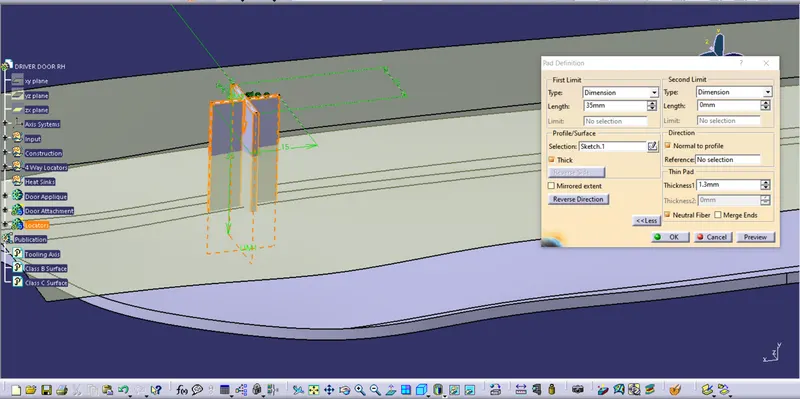
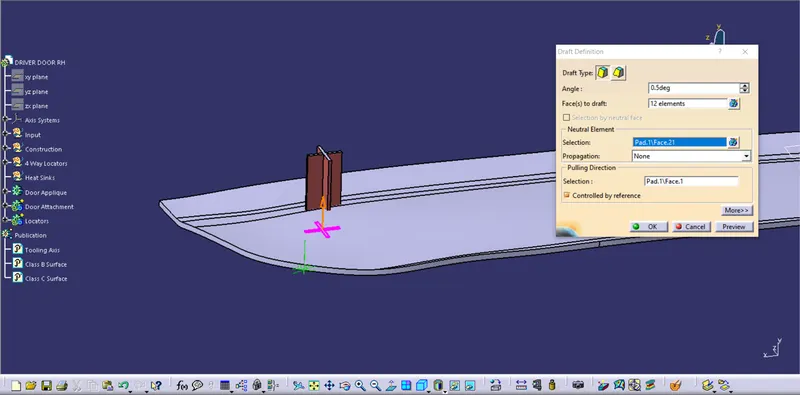
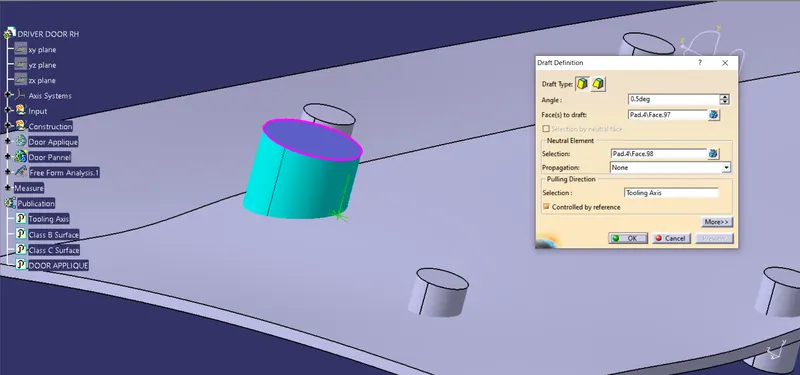
- The locators are drafted by angle of 0.5°along tooling axis
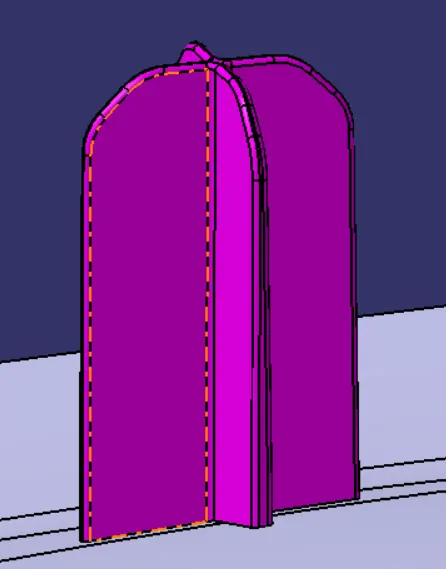
- Entry chamfer and fillets are also applied on the locators
- The locators are designed according to the rib guidelines
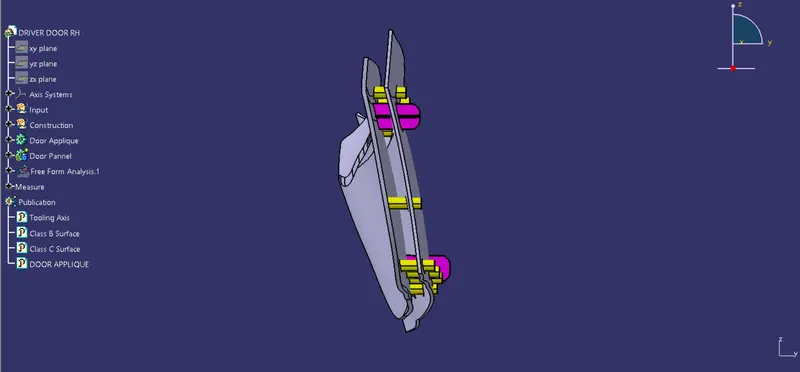
- The height of all the 3 locators w.r.t to the door attachment surface is also maintained at an equal length
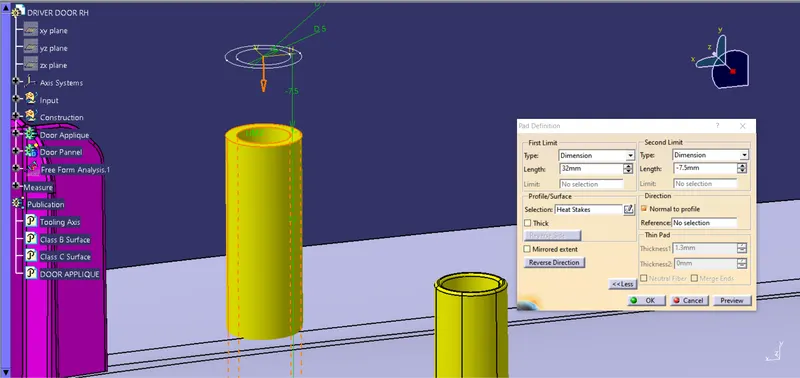
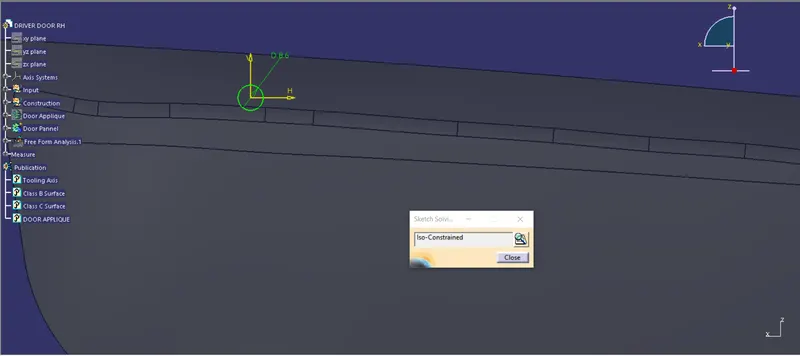
- Heat stakes are created on the door applique surface and their height is maintained at 5mm lower than the locators
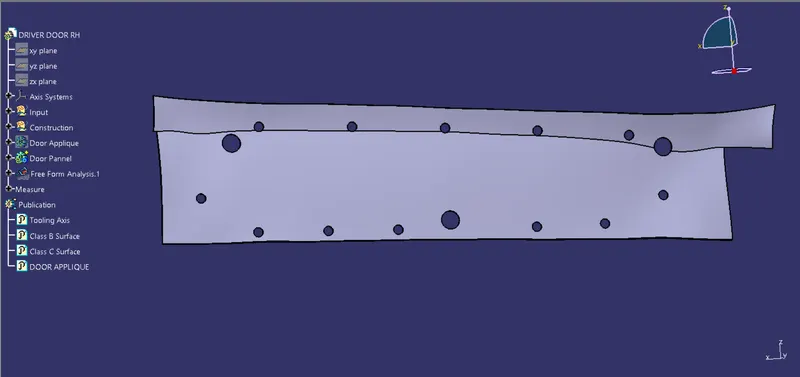
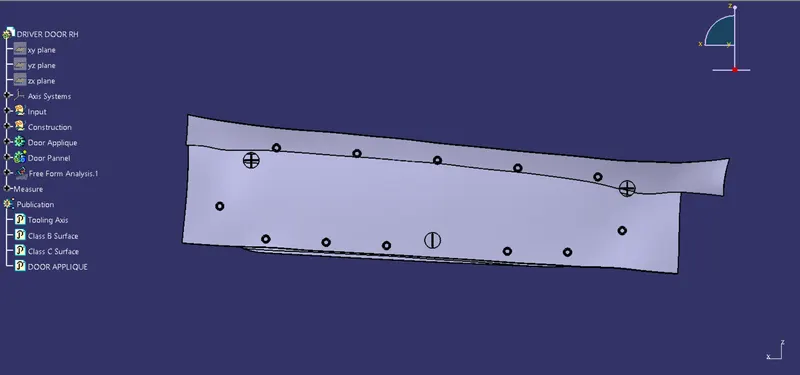
- The heat stakes are position around the boundary of the door applique
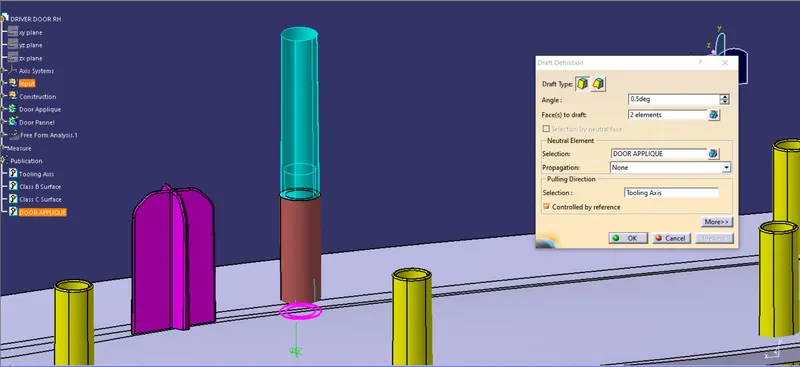
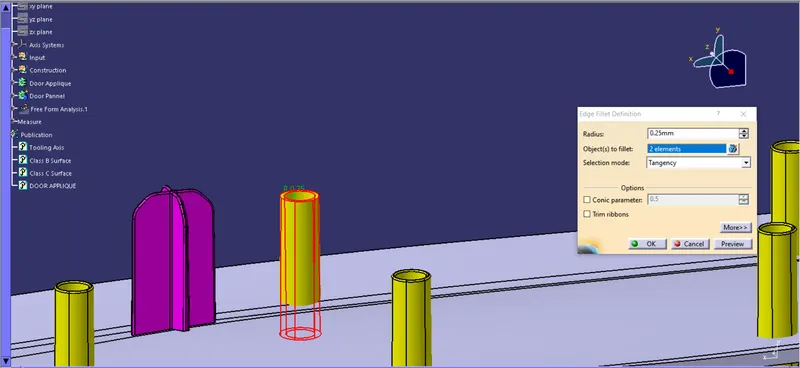
- Each of the heat stakes are also drafted by angle of 0.5°along tooling axis and fillets are applied to them
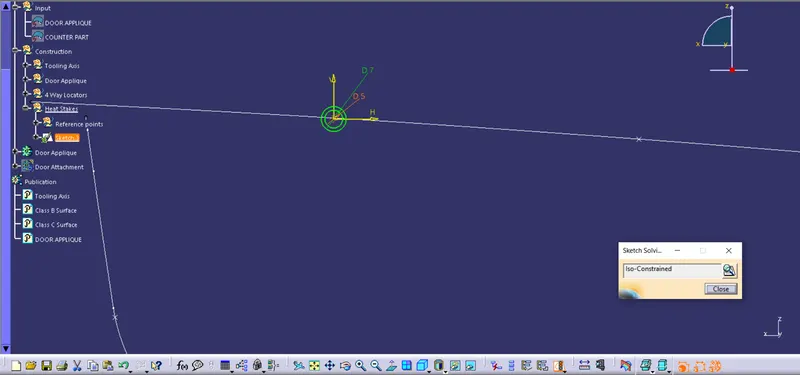
- The sketches of the locators and heat stakes are made on the place ZX plane positioned at the midpoint of the door attachment surface
Locators design
4 way locator skecth
Pad-thicken
Draft
Chamfer and fillets
2 way locator sketch
Heat Stakes design
Heat stakes position sketch
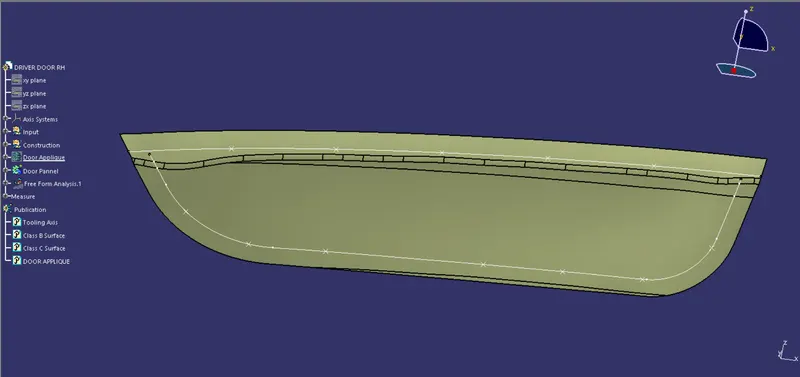
Sketch
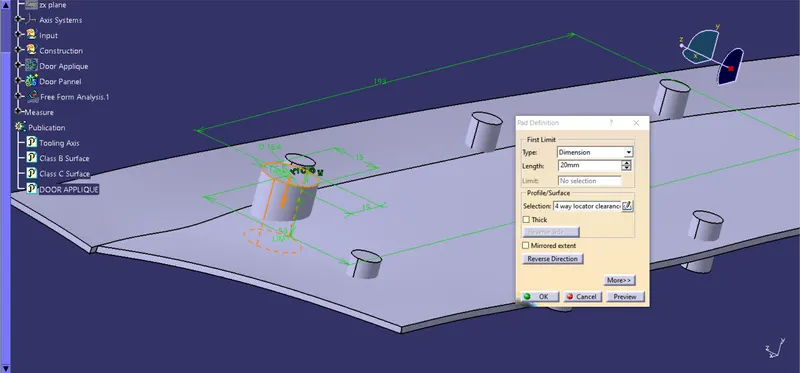
Pad
Draft
Fillets
Counter Clearance on door attachment
- The door attachment surface is thickened by 2mm to create a plastic body
- Clearance for the locators and heat stakes are created on the attachment by removing circular portions around them on the door attachment
- These clearance surfaces are also drafted by 0.5°along tooling axis
- The distance between the clearance surface and the locators and heat stakes is maintained between 0.9 to 1mm
Thickened door attachment
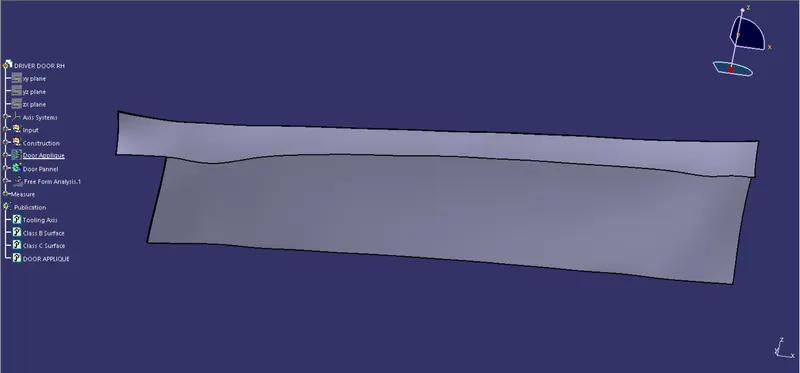
Counter clearance design
Sketch for 4 way locators
Sketch for 2 way locators
Skecth for heat stakes
Pad
Draft
Draft Analysis along Tooling axis
Class A surface
Door Applique with locators and heat stakes
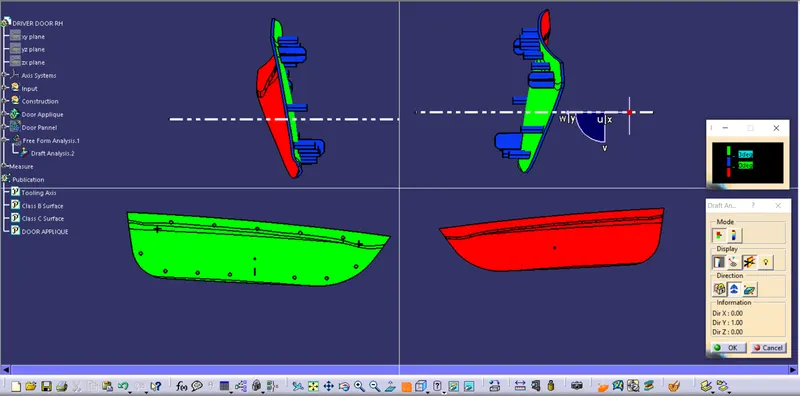
Views of the model
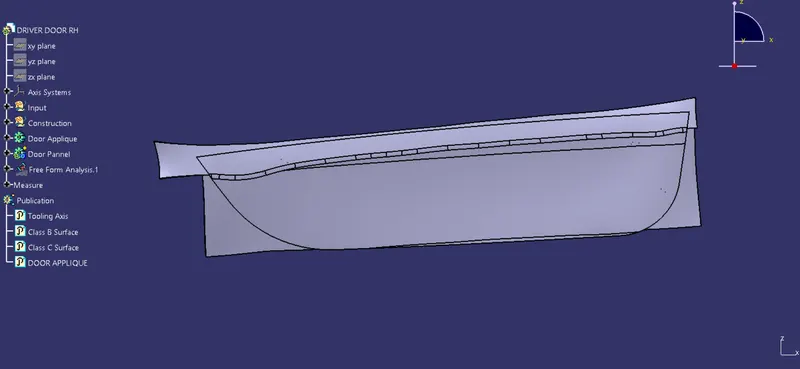
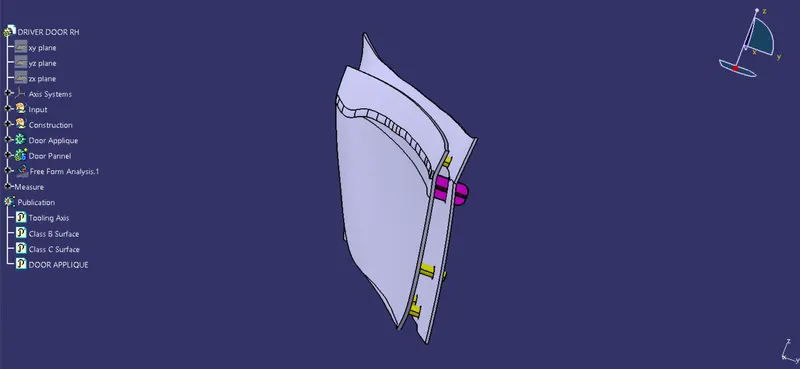
Conclusion
Thus, the door applique was created along with the 4 way an 2 way locators and also the heat stakes.