Design of backdoor
Design of Backdoor
Aim
To design the backdoor of a car using the given class A surface.
Introduction
Backdoor or tailgate is a door, located at the rear of the car, which provides access to the luggage compartment. They are hinged to the body and operated manually or electrically according to the car model.
The doors can be top-mounted, side-mounted or bottom-mounted.The electrically operated back doors are found on premium segment cars.
The backdoors can be mounted in different positions they are given below.
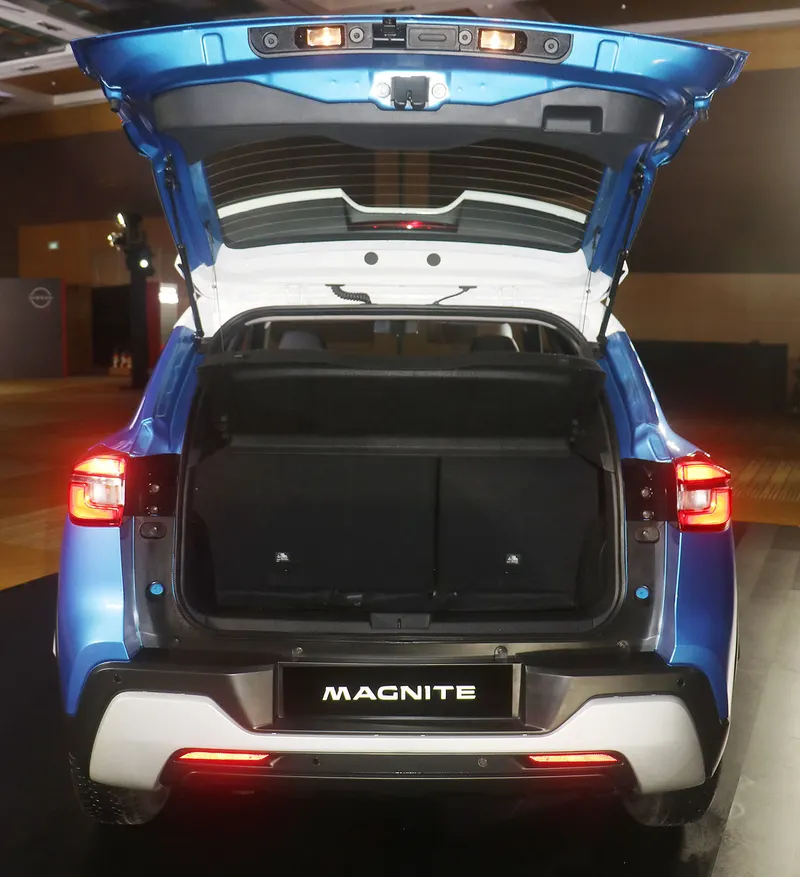
Fig 1. Top-mounted tailgate.
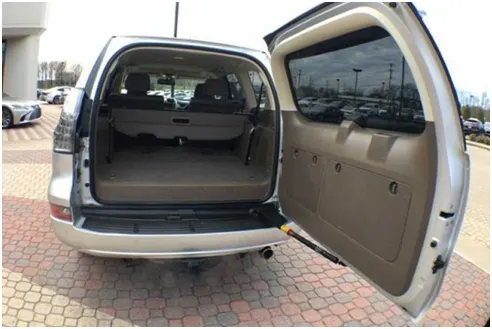
Fig 2. Side-mounted tailgate.
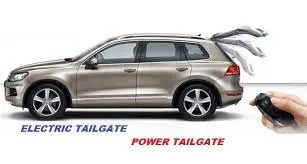
Fig 3. Electrically controlled tailgate
The electrically operated tailgate is seen only in premium car models and most of the other car models use gas stay mounted, manually operated tailgate.
Materials used in manufacturing
The materials commonly used for the tailgate are Steel and Aluminium. The use of steel adds more weight since it is denser than Aluminium. But budget cars are usually dependent on Steel as they are cheaper when compared to Aluminium.
The main differences between Aluminium and Steel are
|
Steel |
Aluminium |
|
Parts are stamped |
Parts are casted |
|
Reinforcements are necessary |
Reinforcements can be neglected |
|
Has only uniform thickness |
Local thickness can be varied |
|
Heavier in weight and more number of components need to be used |
Lighter in weight and less number of components needed |
|
The minimum draft angle is 7°. |
Minimum draft angle is 3° in casted parts which helps in adding luggage space. |
Despite all these benefits, Aluminium is very much costlier when compared to Steel.The permium segment cars uses aluminium as the material for manufacturing.
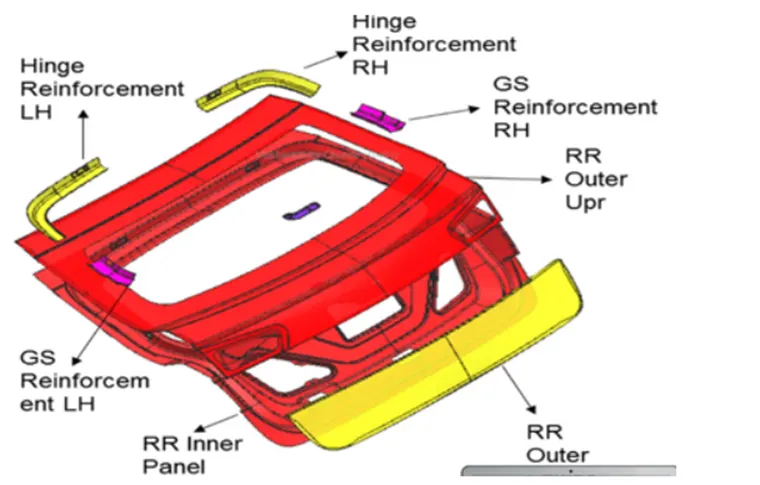
Fig 4. Parts of backdoor when steel is used.
since more components are used it adds up weight and also the spaces are reduced by a small amount.
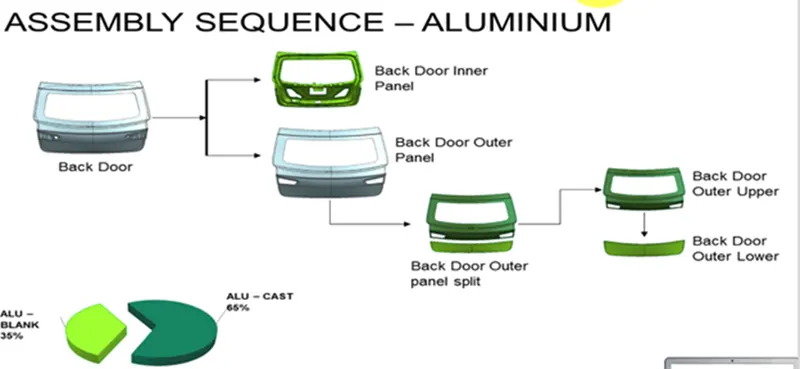
Fig 5. Parts of backdoor when Aluminium is used.
Since no reinforcements are required for Aluminium, the inner panel would be a single, casted part.
Components of a Backdoor
Since back door is an assembly it consists of different components,it is explained below.
- Outer panel or Styling surface
The outer panel is the given Class A surface for designing the backdoor. In this design, the given Class A surface is repaired by bridging the gaps and aand by providing proper blends and sewing of the surfaces. The outer panel can be split into two- Outer panel upper and outer panel lower.
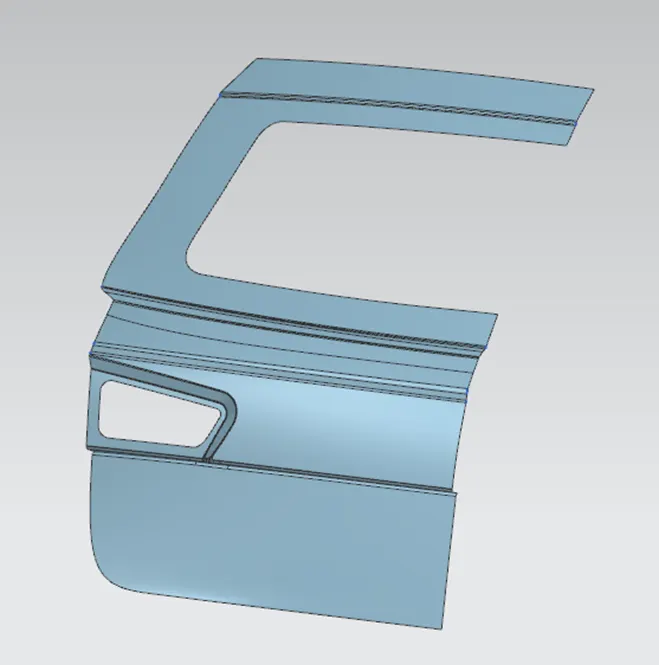
Fig 6. Given Class A surface.
The upper and lower parts of the outer panel are joined together by brazing or spot welding.in most cases brazing process is used.
Brazing is a metal-joining process in which two or more metal sheets or metals are joined together by melting and flowing a filler metal into the joint, with the filler metal having a lower melting point than the adjoining metal. Brazing differs from welding in that it does not involve melting the work pieces.It also helps to maintain the asthetics of class A surface without altering its surface texture.
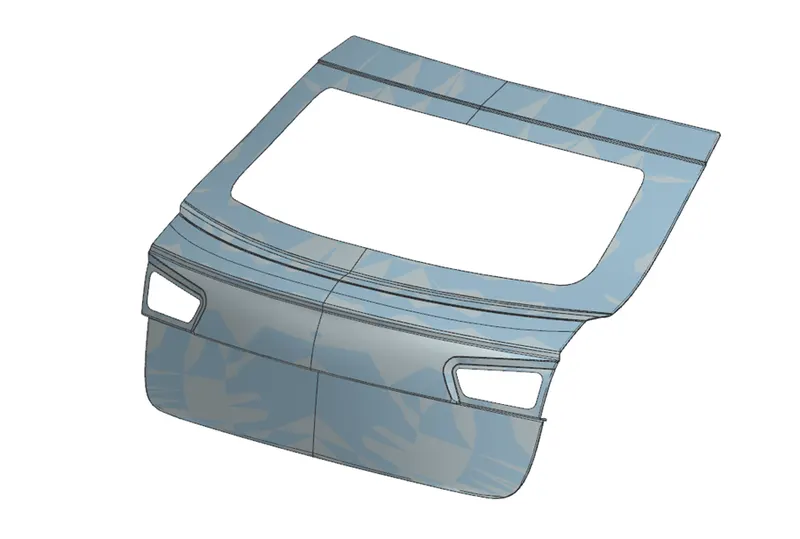
Fig 7. Outer panel upper and lower.
- Inner panel
The inner panel of the backdoor is an essential part which provides strength to it. The mountings of hinges, striker, gas stay and wiper motor are given on the inner panel. The Embosses (V or Y shaped) are given on the inner panel to dissipate the forces acting on the tailgate to the sides of the panel , thereby giving the part more strength and protection from failures. Inner panel is produced by either deep drawing or casting. If steel is used, then deep drawing process is adopted. For deep drawing process of the inner panel , the tooling direction must be given.
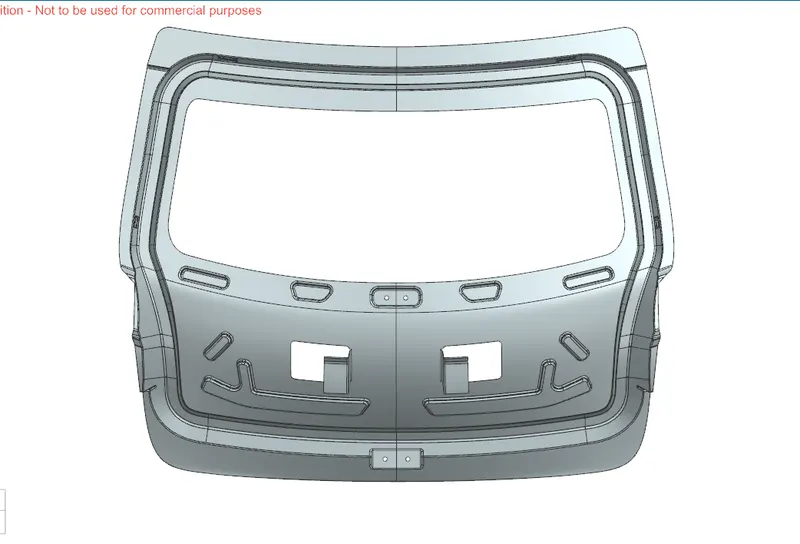
Fig 8. Inner panel
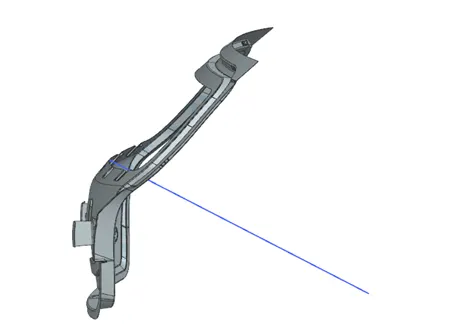
Fig 9. Tooling direction.
3 Sealing Flange
Sealing Flange is the section of the inner panel which enables the backdoor to sit over the rear body side of the car. its is also a main part of the back door as it decides how a backdoor is mounted on the rear body side of the car and also restricts any external matter to enter inside the vehicle like moisture ,dust or snow.
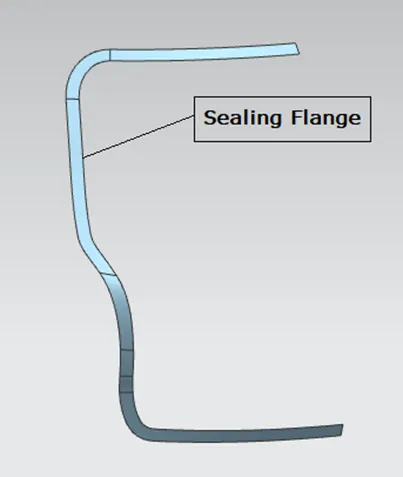
Fig 10. Sealing flange.
The inner panel a extended surface is also given to join the inner panel to the outer panel with mastic and proper clearance is also given between the inner and outer panel.It also increases the strength between the stuructures and also reduces vibrations.
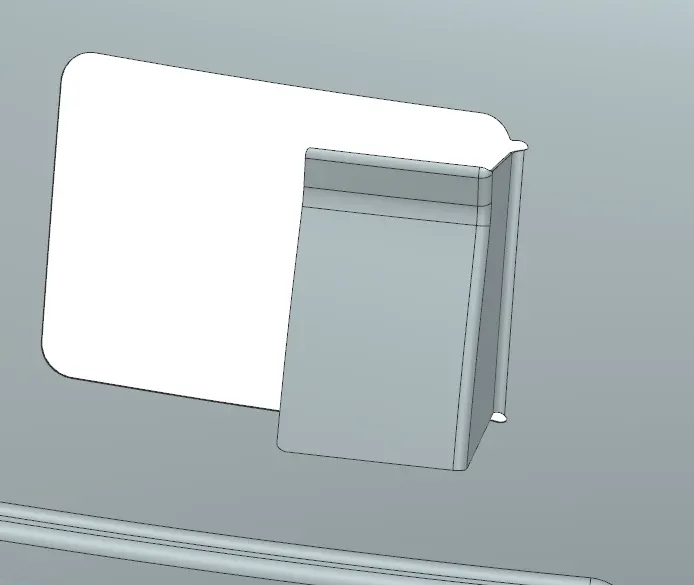
Fig 11. Flange for mastic sealant.
4. Reinforcements
Reinforcements are added on local regions where forces occur to improve the strength of the panel and to withstand the additional forces that occur on those regions. Hinge reinforcement, gas stay reinforcement, wiper motor reinforcement and striker reinforcement are given in this design to provide additional strength . They are deigned as separate parts in the assembly.
Hinge reinforcements
Hinge reinforcements are given for both the left and right hinges. Hinge is a pivot on which the backdoor rotates while opening and closing.
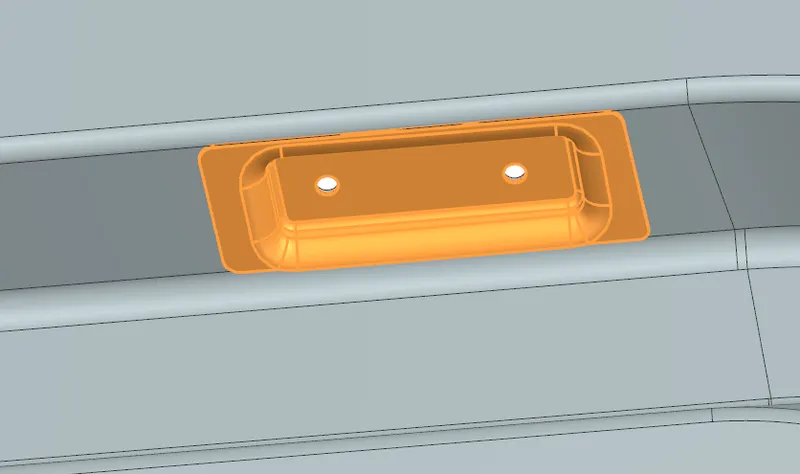
Fig 12. Hinge reinforcements.
Gas stay reinforcements
Gas stay reinforcements supports the backdoor while opening or closing and it helps to keep the backdoor firm in its open position witout sagging . A hydraulic piston arrangement is commonly used for backdoor. Reinforcements are given on both sides.
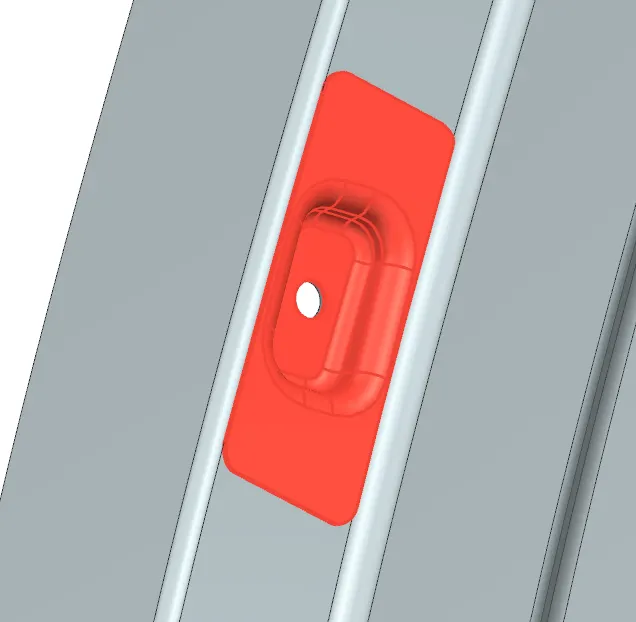
Fig 13. Gas stay reinforcement.
Wiper motor reinforcement
The motor for rear wiper is mounted on the tailgate. In order to provide strength and to avoid deformations due to the heating of motor and to improve the NVH, reinforcements are provided for the wiper motor area in the inner panel.
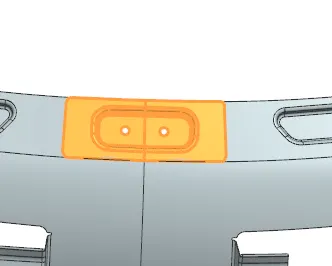
Fig 14. Wiper motor reinforcement.
Latch and striker reinforcement
This reinforcement is given at the bottom portion for positioning the latch and striker. This reinforcement helps in withstanding the forces due to the over slamming of the backdoor during opening and closing of the door.
This reinforcement is given according to the the hinge axis and the trajectory of the backdoor. A circle is drawn, with the hinge axis as its centre and the striker is positioned along the circle, which is the trajectory of the backdoor.The stricker is placed perpendicular to the trajectary axis.
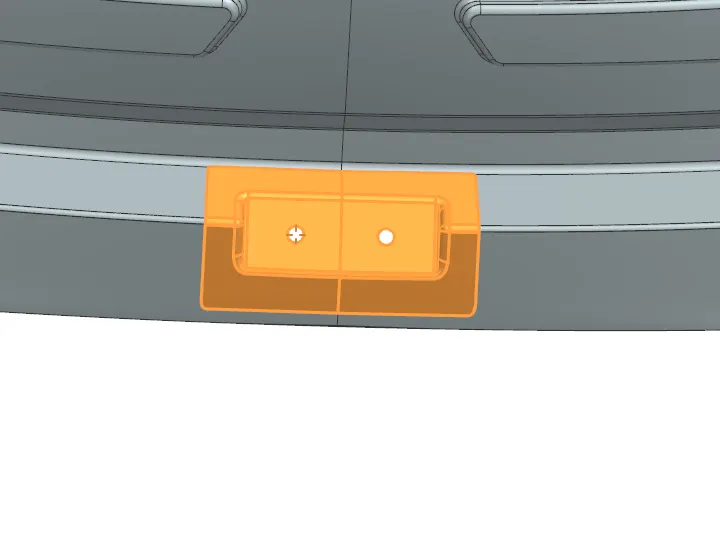
Fig 15. Latch and striker reinforcement.
Manufacturing processes used
Deep drawing:
Manufacturing processes adopted
Deep drawing: Deep drawing is a sheet metal forming process that involves complex material flow and force distributions. It is a shape transformation process with material retention. The process is called deepdrwing process because the depth of the part exceeds its diameter.
The process involves the drawing of a metal sheet blank into a forming die by the action of a mechanical force using a punch.Deep drawing process is adopted for the manufacturing the backdoor using Steel.
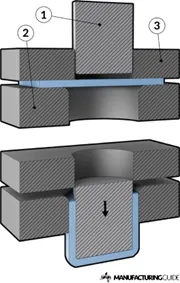
Fig 16. Deep drawing process
Hemming
Hemming of the outer panel in the backdoor of a car refers to a specific manufacturing process used to finish and shape the edge of the metal panel. In automotive production, the outer panel of a backdoor typically consists of a sheet of metal that needs to be folded and joined to create a seamless, aesthetically pleasing appearance.
In the backdoor design hemming is done between the outer and inner panel in which the outer panel is wrapped to inner panel.The clearnc of 0.02 mm is provided for the sealent between the two surfaces to fill the gaps.
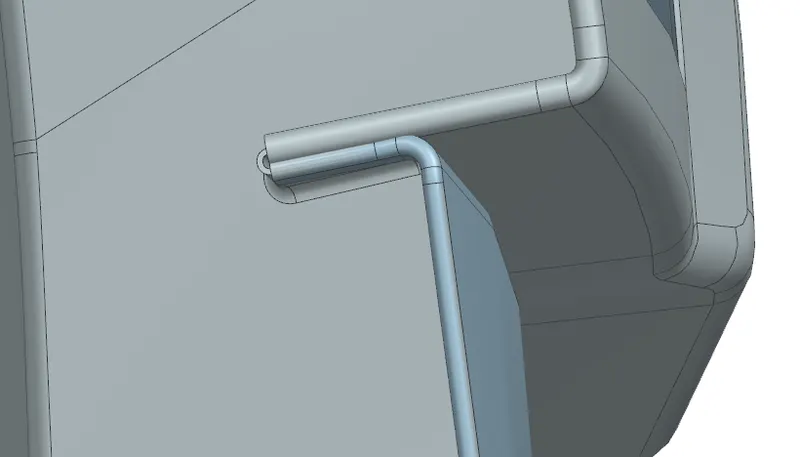
Fig 17. Hemming done for outer panel.
During the hemming process reliefs are provided at the corners of the panel to prevent stress concentrations and vibrations due to the rolling action of hemming rollers over the panel.
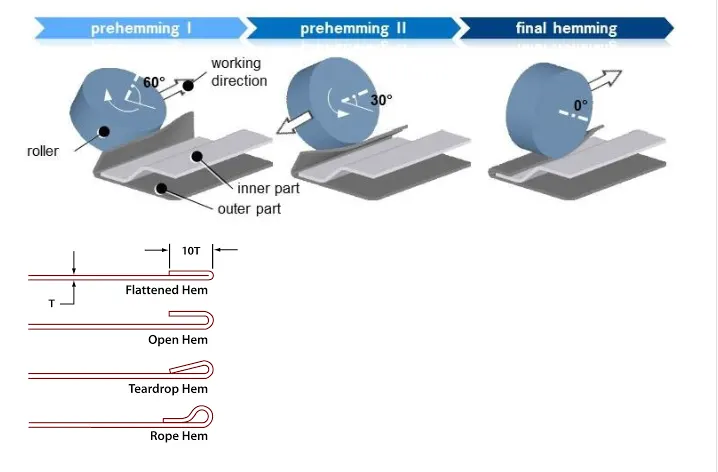
Fig 18. Hemming done using rollers
Analysis of backdoor
Load Analysis
The part is subjected to various load conditions which are subjected and determined whether they return to the original position.
Bend test: In the bend test of the backdoor all the four corner regions are constrained, and load is applied along the centre region.
Torsion test: The top two corner regions and the striker emboss region is constrained, and load is applied at the two corners at the bottom in opposite direction.
Abuse cases: The door is subjected to conditions like over slamming, hanging on the door, like resting the hands on the door and analysed.
Dent test: Dents are created on the surface and tested.
Assembly load case: The various forces that are likely to occur during the assembly of the vehicle are exerted and tested whether the tailgate is able to withstand them.
Endurance test: Here the backdoor is opened and closed a particular number of cycles and their workability of the part is determined.
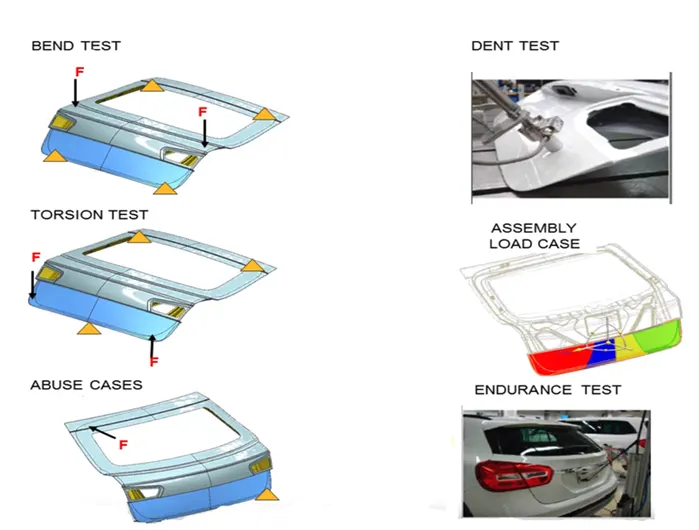
Fig 19. Different types of load tests.
Draft analysis of backdoor
Draft analysis is done for the inner panel for ensure whether the manufacturing of the panel can be done by deep drawing process.
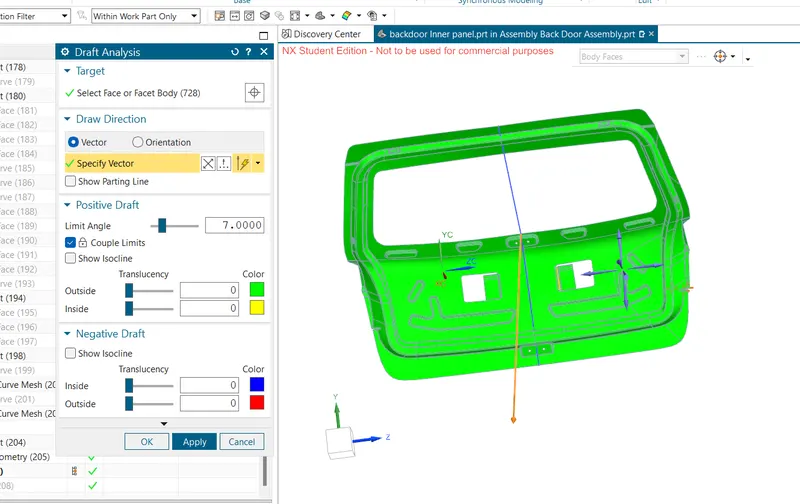
Fig 20. Draft analysis of the innerpanel.
Conclusion of the design
After the hemming, mirroring and sewing of the surfaces and required thickening of the parts, the final backdoor assembly design is completed.
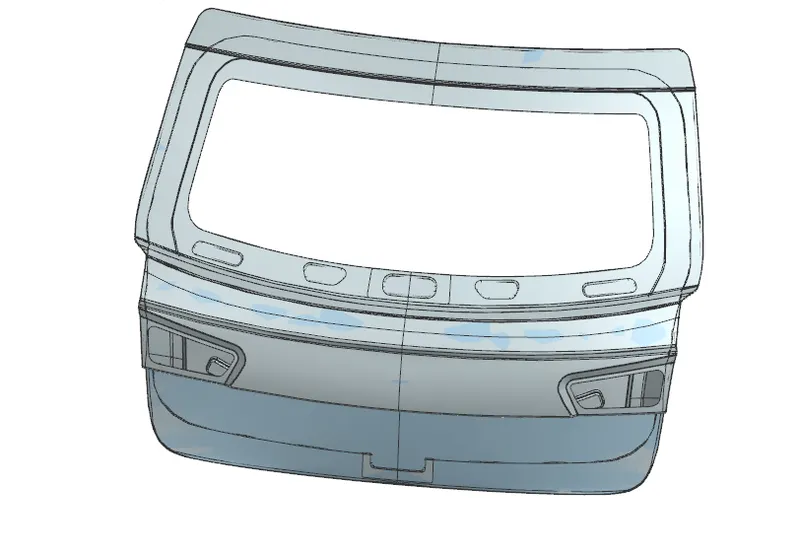
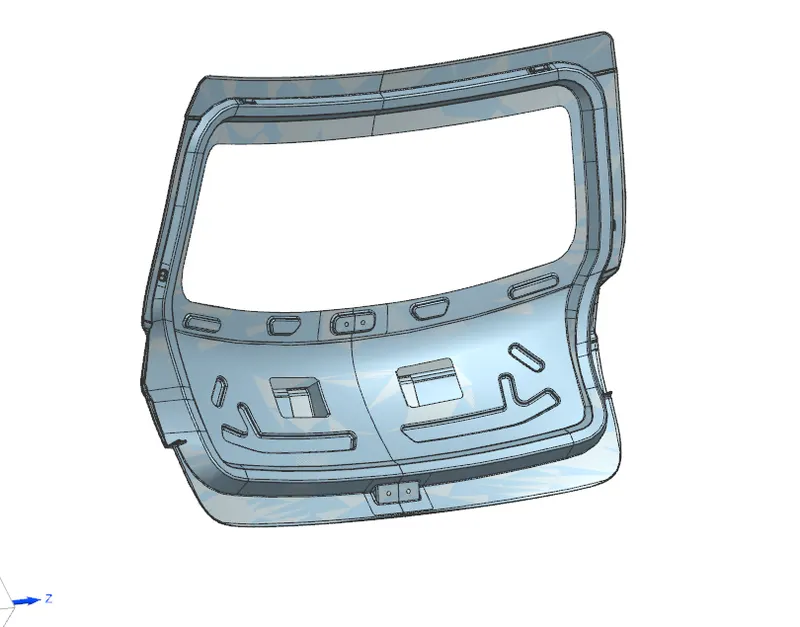
Fig 20&21. Final assembly design of the backdoor.