Design of backdoor
1.AIM
Use the provided styling surface to come up with a back door design, use appropriate design methodologies, and provide the necessary reinforcements and embosses
2.INTRODUCTION
2.1 BACK DOOR
Back door or tail gate simply refers to the back of the car that can open and close.it covering the rear of the vehicle.It provide access to a cargo area (trunk/boot ).A tailgate hinged at the roof is a predominant characteristic of hatchbacks, estates/station wagons and liftbacks .The door or opening of a cargo area may be hinged at the top, side, or bottom.
In most cars, usually this process will be done manually. One has to get down the car to open and close the tail-gate with the car key.Nowadays, automobile manufacturers providing Advanced features like the automated tail-gate. An automatic tail-gate in the car will do the process of shutting and opening the tail-gate electronically.
Types of Back Door in a car:
- Top Mounted door
- Side mounted door
- Bottom Mounted Door
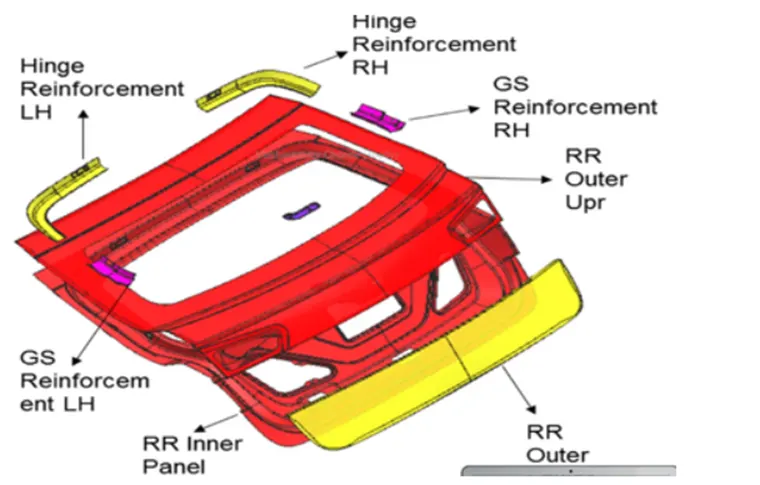
Components of Back Door:
Manufacturing Process of Back Door :
1.Blanking
When required, blanking is the first step of the stamping process. Blanking is the process of cutting larger sheet or coils of metal into smaller, more manageable pieces. Blanking is usually performed when a stamped metal piece will be drawn or formed.
2.Piercing
If a part requires slots, holes, or other cutouts, piercing can be employed. Piercing, which can be performed simultaneously with blanking, punches the requisite shapes out of the metal sheet.
3.Drawing
Drawing is the actual stamping in the metal stamping process. A punch forces a section of metal through a die, providing the primary shape of the part. When the depth of the part is less than the primary opening, it is considered shallow drawing; parts with a depth greater than the opening are deep drawn.
4.Bending
Bending is a fairly self-explanatory process. The part-in-progress is placed on a specially designed die and a ram pushes against the metal, providing the required bend. Bending is performed after drawing, as attempting to punch an already bent piece of metal causes the entire part to deform.
5.Hemming
Hemming is a technology used by the automotive industry to join inner and outer closure panels together (hoods, doors, tailgates, etc.). It is the process of bending/folding the flange of the outer panel over the inner one. The accuracy of the operation affects significantly the appearance of the car’s outer surfaces and is therefore a critical factor in the final quality of a finished vehicle.
6.Roller hemming :-The robotized hemming systems use a standard industrial robot integrated with a roller hemming head, offering a very flexible solution. This roller hemming head consists of a body, some guides and a number of rolls that are designed according to the geometry of the part in each case.
PARTS OF BACKDOOR
- Back door outer panel (upper and lower)
- Back door inner panel
- Hinge reinforcements
- Gas stay reinforcements
- Latch and striker reinforcements
- Wiper motor reinforcements
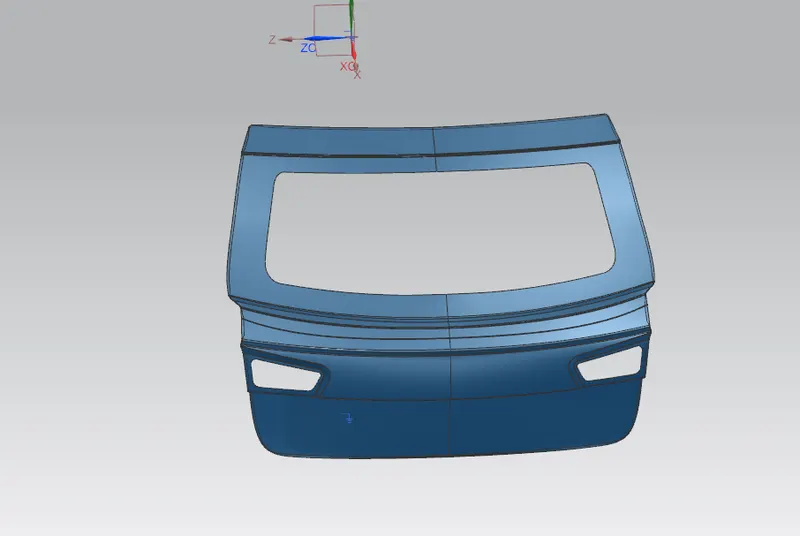
1. BACK DOOR OUTER PANEL
In this design back door is created as two different parts back door outer panel upper and lower. This outer panel designed based on visibility criteria and proper reliefs provided at the corner for hemming operation .The thickness of outer panel is 0.75 mm.
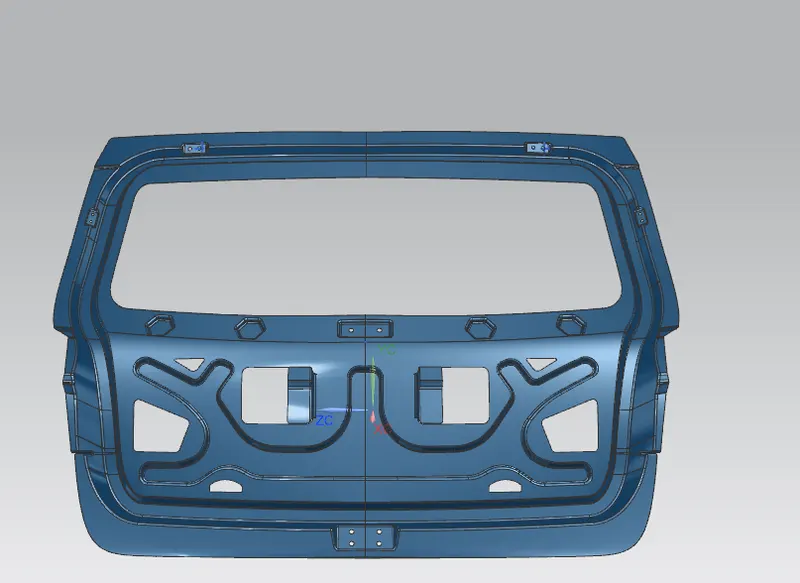
.BACK DOOR INNER PANEL
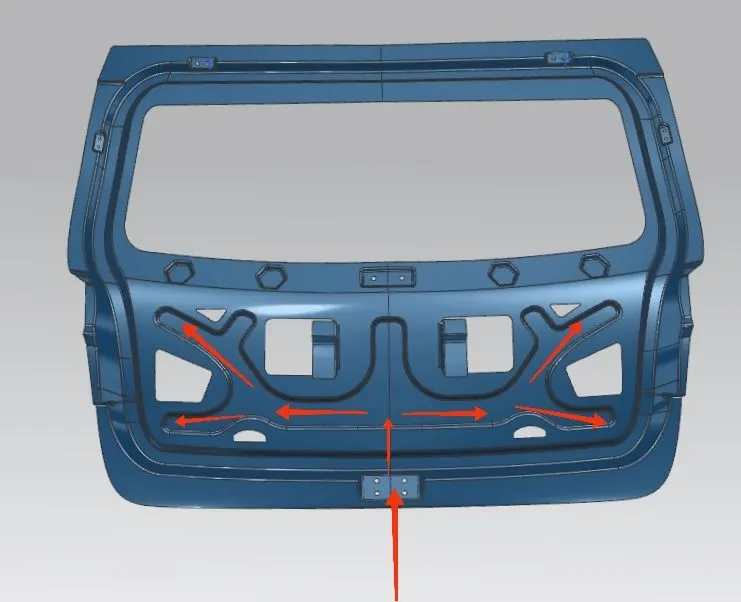
Back door outer panel designed based on hinge, gas stay, wiper motor position and reinforcement as well as visibility criteria .Suitable tooling direction is created for trouble free manufacturing process.In this design stamping operations created based on this tooling direction. Embosses are provided in this design for force dissipation. In this design appropriate clearance given in mastic areas .The inner panel thickness is 0.75 mm
- Force dissipation
This inner panel design created by considering the force dissipation criteria.The embosses are created in such a manner that force will dissipate in to sides of the back door during a collision and prevent reaching inside the passenger cabin.Y and V embosses provided in the back door for force dissipation and improve the strength of the metal.
- Hinge reinforcement
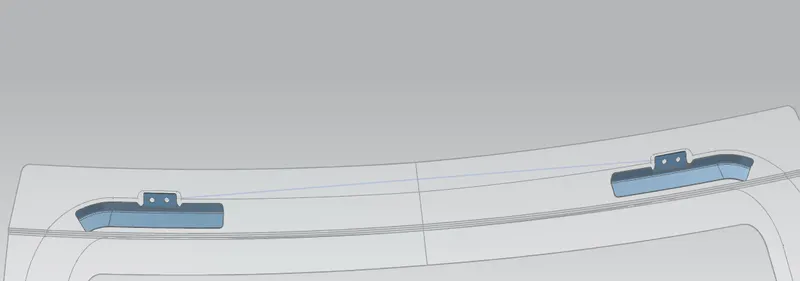
In this design hinges provided on the top side of the door. Appropriate reinforcement given for hinge mounting areas to improve the strength.
- Wiper motor reinforcement
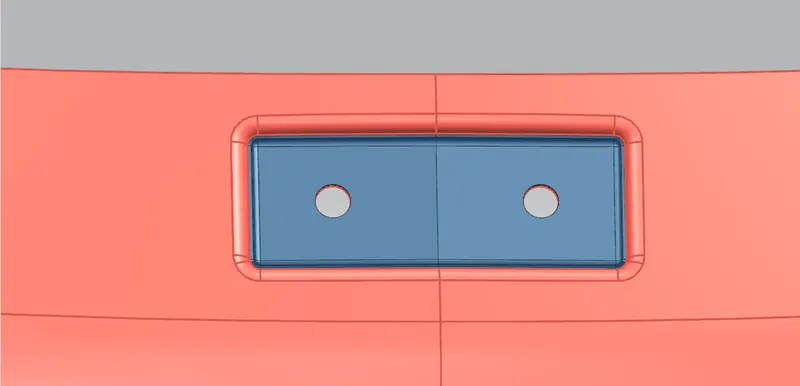
Reinforcement provided in this region for fixing the wiper motor.
- Latch and striker reinforcement
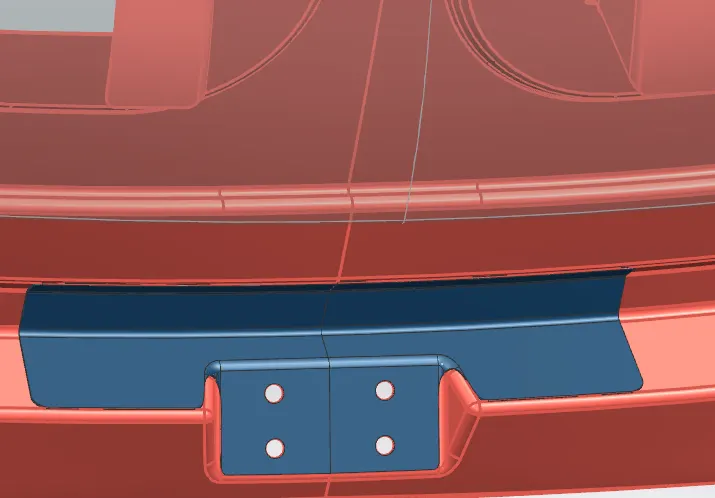
The striker is designed to create a tight fit between the door and the seal on the cab. The door open and shut several times in a day.So more force acting on this area.The reinforcement given in the latch and striker mounting area to increase the strength.it is spot welded on the inner panel
- Latch and striker reinforcement
The striker is designed to create a tight fit between the door and the seal on the cab. The door open and shut several times in a day.So more force acting on this area.The reinforcement given in the latch and striker mounting area to increase the strength.it is spot welded on the inner panel
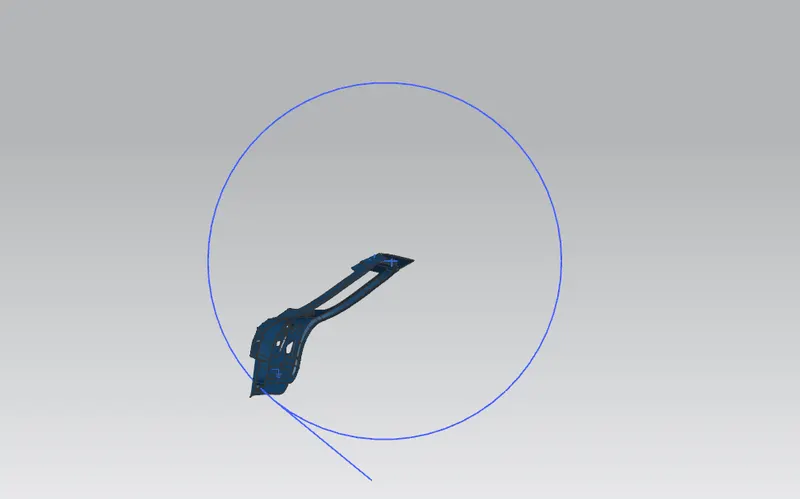
- trajectory
The trajectory is created to position the latch and striker .latch system must be able to catch the striker of the door the while closing. Circle is drawn from the hinge axis. The striker follow this path.
- Hemming
Hemming is a technology used by the automotive industry to join inner and outer closure panels together (hoods, doors, tailgates, etc.).In addition adhesive bond provide for excellent joining of panels it also reduce vibration .here this design 0.2mm clearance provided for hem glue.
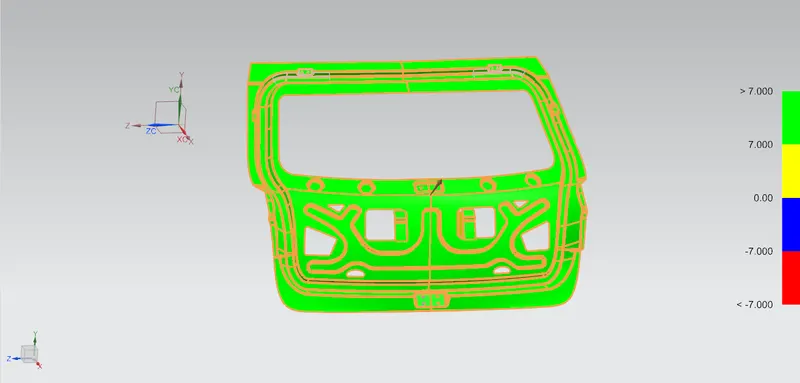
5.0 Draft Analysis
draft analysis performed to check the designed part is suitable for stamping operation with respect to the tooling direction.We can find out the errors by using this feature.The minimum draft angle is 7.The negative draft is denoted by different colour so we can easily find out the unsuitable areas.