Core & Cavity Design for a plastic switch bezel component using Catia v5
CORE AND CAVITY DESIGN FOR A PLASTIC SWITCH BEZEL COMPONENT USING CATIA V5
OBJECTIVE
-
To perform draft analysis on a Class-A Surface model of a Switch Bezel component and create a solid model from the Class A surface using B and C surfaces
- To create the following features with respect to the molding process of the Switch Bezel component:
- Parting surface
- Core Block
- Cavity Block
- Parting line
INTRODUCTION
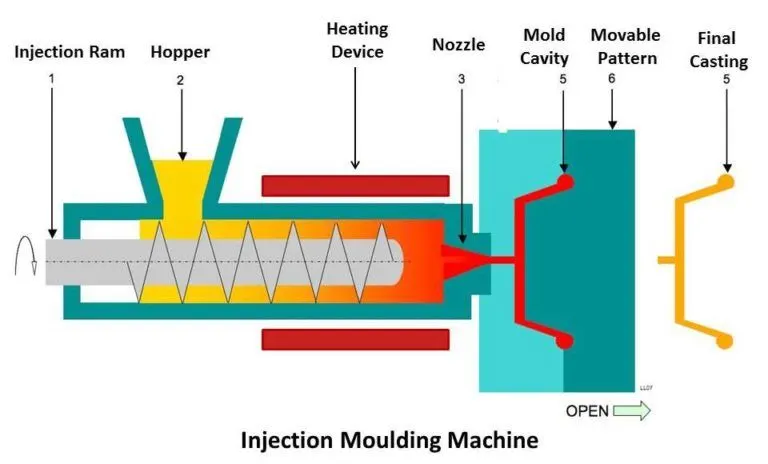
Injection Molding
It is a manufacturing process used for the mass production of plastic components. It works by injecting molten material (plastic) into a mold. Under the application of heat and pressure, the material solidifies into the required shape. Once the product cools, it is ejected from the mold with the help of ejector pins.
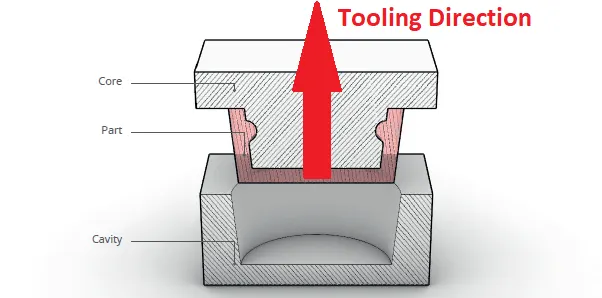
Tooling direction
The direction along which the core pulls apart from the cavity is termed as the Dyeline or the Tooling direction.
Draft
To facilitate easy removal of components from the mold, it is necessary to add a taper all along the surface with reference to the tooling direction. This taper is termed as a draft and its value ranges from 0.5 degrees to 3 degrees, with the latter being the most widely accepted norm.
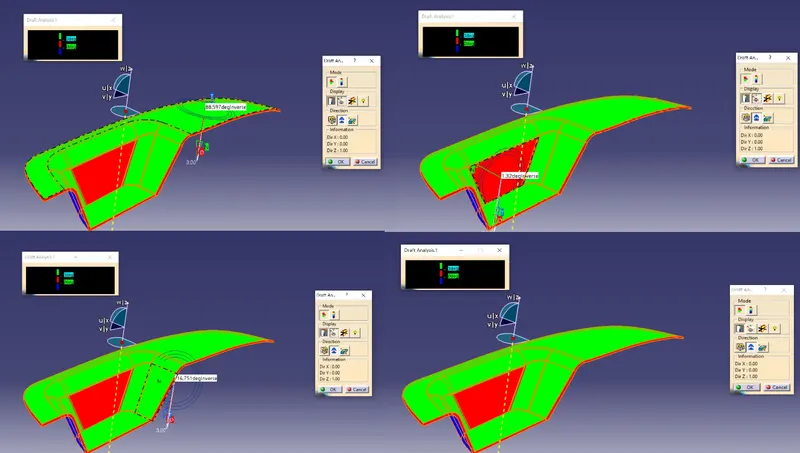
The Draft analysis command in CATIA enables to detect if the drafted part can be removed in an easy manner. This analysis is performed based on colour ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
Class-A Surfaces
The aesthetic/free-form surface which constitutes the visible outer layer of a component can be termed as a Class-A Surface. In this project, the Class-A surface of a Switch bezel model which is composed only of curvature continuous surfaces is used as the input for performing the draft analysis.
B and C Surfaces
The B surface forms the inner components and acts as a base for the Class-A surface. C surface connects the A and B surfaces and thereby provides a thickness for the final component
Core and Cavity
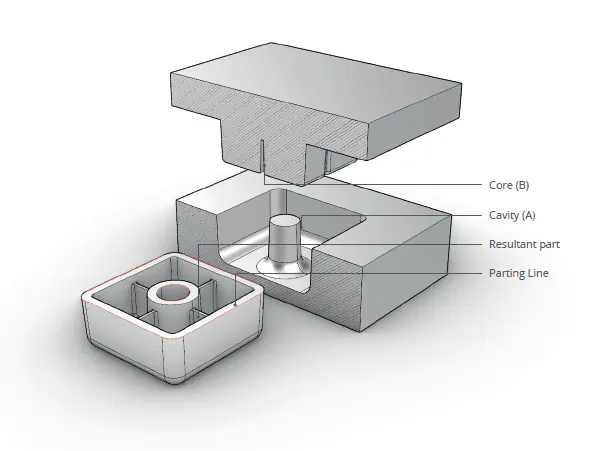
In a typical injection molding machine, one half of the mold (the A-side) is attached to the fixed side of the press, and the other half of the mold (the B-side) is attached to the moving clamp side of the press. The clamp (or B) side contains the ejection actuator, which controls the ejector pins. The clamp forces the A and B-sides together, molten plastic is injected into the mold and allowed to cool, the clamp pulls the B-side of the mold away, the ejection pins are actuated, and the part releases from the mold.
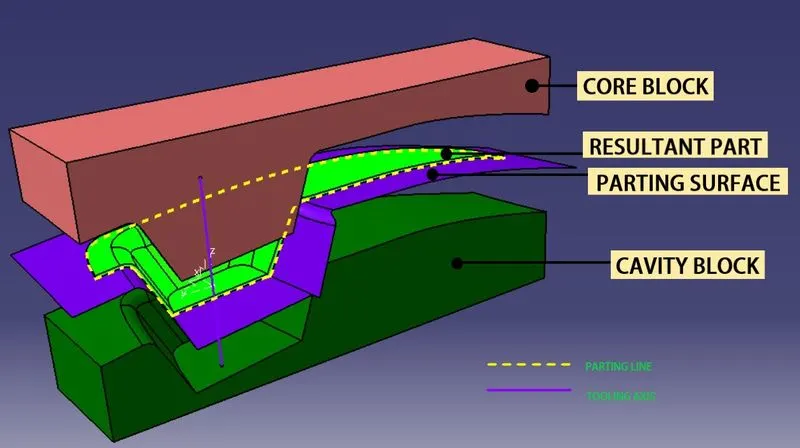
The A- side of the mold is known as the Core and the B- side of the mold is known as the Cavity. The surface which forms the interface between the core and cavity is known as the Parting surface and the boundary of this surface is termed as the Parting line.
OVERVIEW OF THE PROJECT
BISECTING LINE METHOD
Since draft is measured with reference to a tooling axis, the first step after importing the model into CATIA was the creation of a tooling axis. To incorporate for tool clearances due to the presence of tapered surfaces in the part, the bisecting line method was used to create the tooling axis.
After converting the surface into a 2D profile using the Intersection command from the surface workbench, two inclined lines were created using the endpoints of the 2D curves which represented the tapered faces. Using a bisecting line type, a third line was created along the centre point which signified the coincidence of the tapered faces. This line was the required tooling axis for this component.
DRAFT ANALYSIS
The draft analysis command in CATIA helps to detect whether the drafts provided in the model will facilitate easy removal of the component during manufacture.
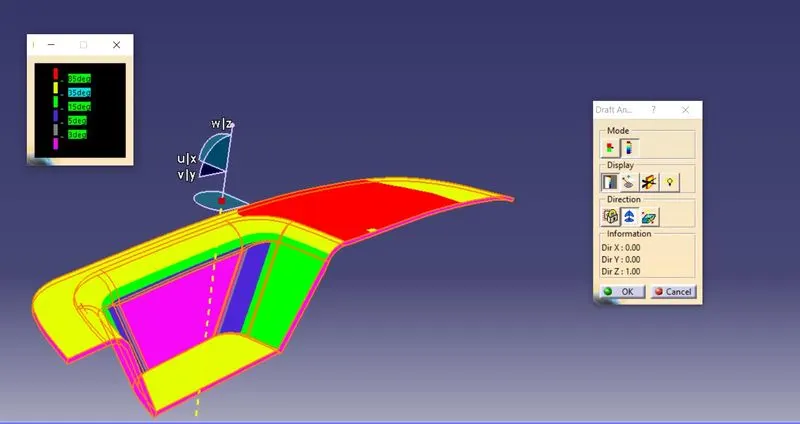
This analysis is performed based on colour ranges identifying zones on the analyzed element where the deviation from the draft at any point, corresponds to specified values.
-
When the draft angle value of the surface is equal or smaller than a graduated value, the color below the graduated value is applied
-
When the draft angle value of the surface is greater than the greatest graduated value, the color above this graduated value is applied
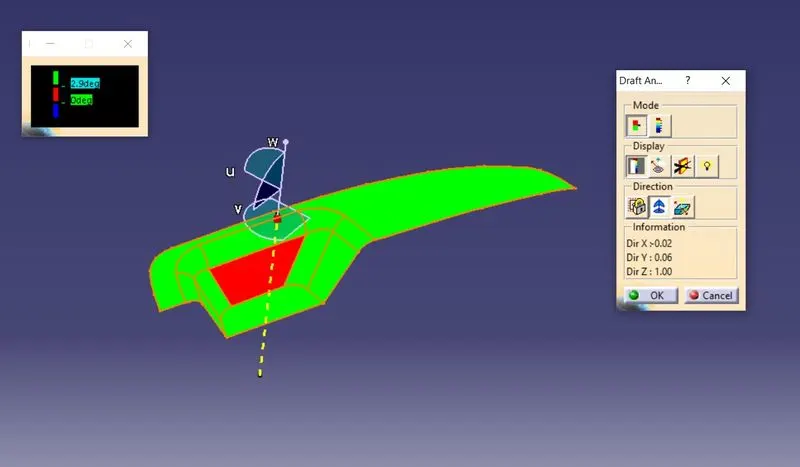
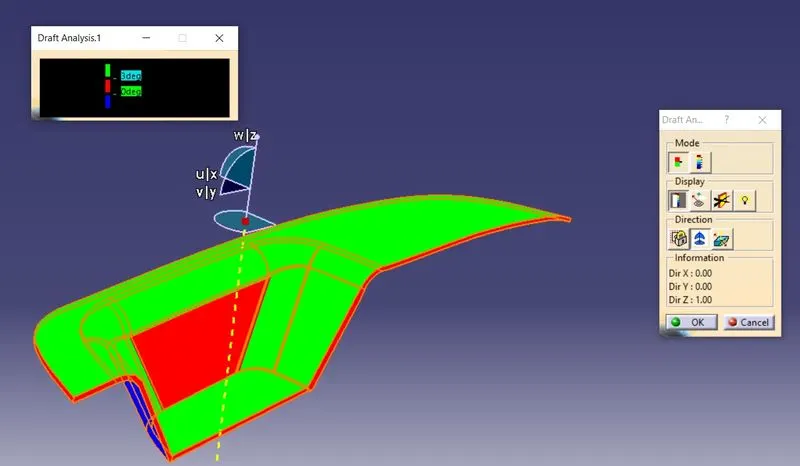
In this project, the required draft for all surfaces were chosen as 3 degrees and hence the quick mode option in draft analysis was chosen which incorporated two different colours for two input values.
B AND C SURFACE CREATION
The B surface was created by offsetting the Class-A surface and then extrapolating it to accommodate the entire area of the Class-A surface.
The C surface provided the thickness and acted as the joining surface between Class A and B surfaces.
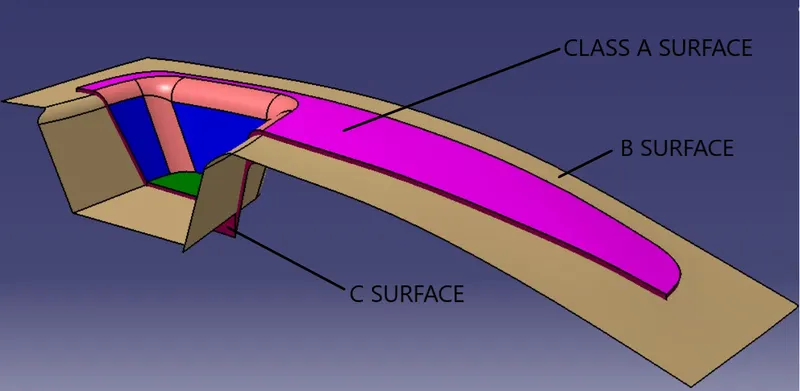
The Class A and C surfaces were made into a single surface using the Trim command in the surface workbench. This was then trimmed using the B surface to create the final component. The model was then converted into a solid using the Close Surface command.
CORE AND CAVITY BLOCKS CREATION
The Class A surface was extrapolated and then trimmed with the C surface to create the parting surface. This surface was trimmed with an Z axis rectangular sketch extrusion and made into a solid body to create the Cavity block. The same extrusion was trimmed with the B surface to create the Cavity block.
DETAILED PROCEDURE
1. Importing the Class-A Surface
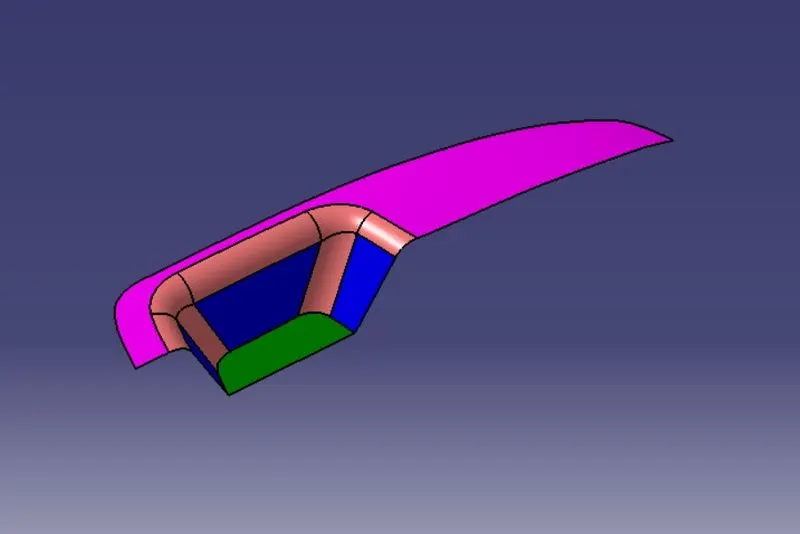
- The surface model of the Base Bracket was imported into the CATIA workspace for further procedures
- Using the Join command in the surface workbench, the surface was checked for any continuity errors
2. Creation of the tooling axis
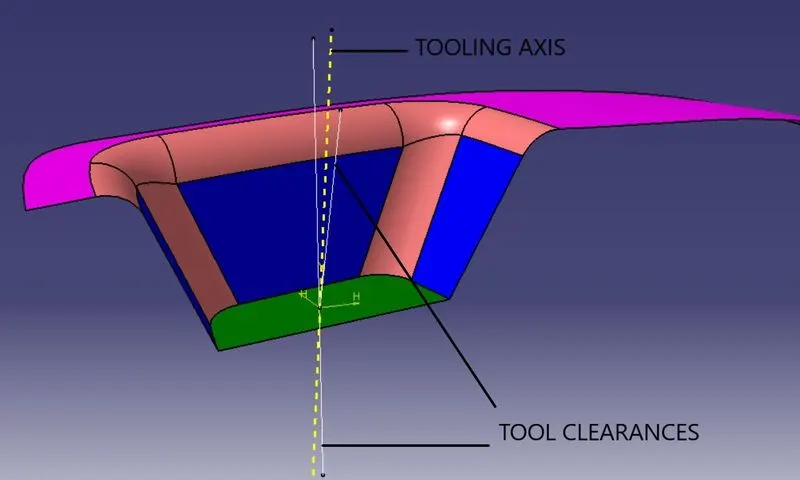
- For creation of a proper tooling direction, the pocket in the model needed to be addressed with the help of a separate tool clearance in the YZ and XZ plane
- Intersection curves of the the model were used to create lines which represented the inclined faces of the pocket
- In the YZ plane, two inclined faces were used as a reference for two inclined lines and using the bisecting line tool, a line which passed through the centre point was created
- For the XZ plane, due to the presence of only one inclined line, a line was drawn through the centre point and dimensioned to be at an appropriate angle (3 degree, later changed to adjust the tooling axis)
- Using both these lines as a reference in the bisecting line tool, a new line was created which represented the tooling axis of the model
3. Creation of B Surface
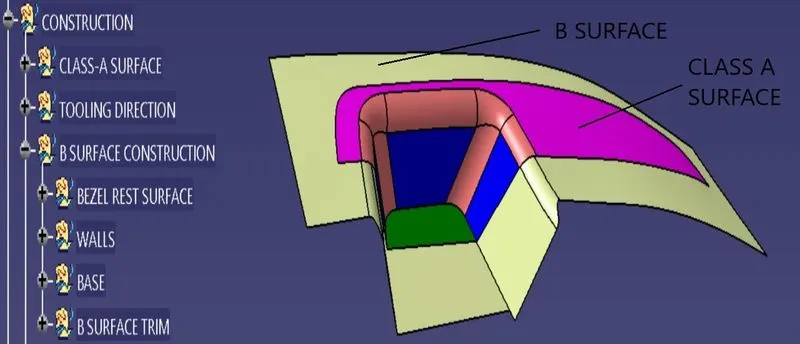
- The Class A surface was used to extract various surfaces for the creation of B surface
- The top area, which represented the Bezel rest surface was first extracted using the Extract tool and then separated from the existing constraints using the Untrim tool
- Similar procedures were repeated for the walls and base of the pocket
- All these surfaces were modified using the Extrapolate tool and the offset to the required thickness specification of the project which was 2.5mm
4. Creation of C Surface
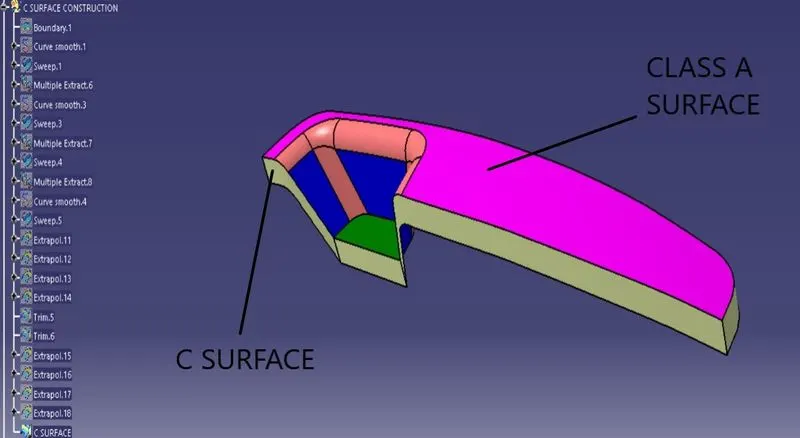
- The outside boundary of the Class A surface was chosen and converted into 2D profiles using the Boundary command
- Since C surface connects both the A and B surface, it essentially signifies the thickness and hence the Swept Surface command was used to create it
- To ensure proper smoothness for the curves, the Smooth curves tool was used to create continuous curvature
5. Creating the final trim
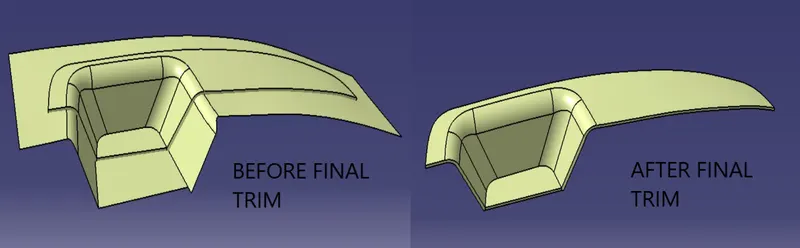
- To ensure that no gaps were present between the combined Class A and C surfaces, the surfaces were extrapolated and then trimmed
- This trimmed model was then further trimmed using the B surface to create the final closed surface model of the switch bezel
6. Converting the surface model into a solid model
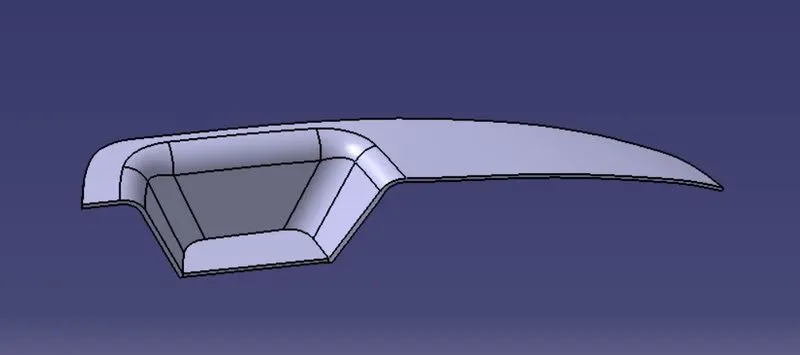
- To complete the model, the Close Surface command from the part workbench was used thereby creating a solid model
7. Performing the draft analysis on the final plastic component
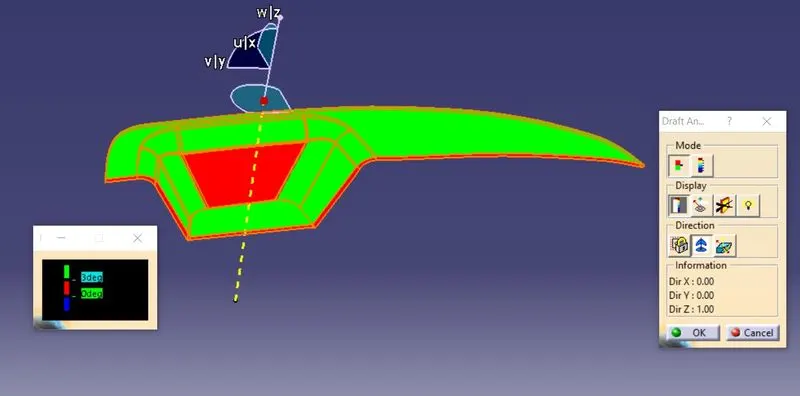
- The draft analysis was then performed on the plastic component using the Feature Draft Analysis tool
- The draft direction was chosen by dragging the compass and coinciding it with the tooling axis
- The quick analysis mode was chosen since the draft value chosen for this project was 3 degrees for all the surfaces of the component
- A light green colour was chosen to represent a minimum 3 degree draft and all the surfaces successfully returned proper results
8. Creating the parting line and the parting surface
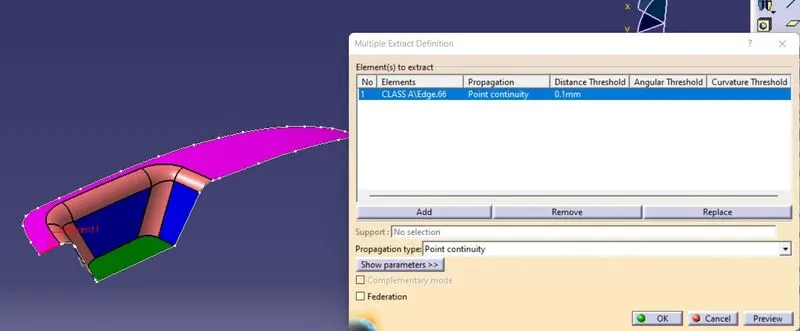
- The outer boundary of the Class-A surface was extracted using the multiple extract tool
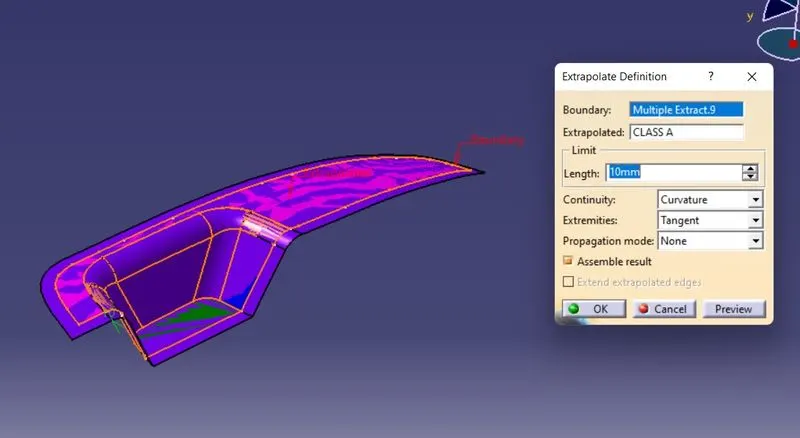
- The surface was then extended by using the extrapolate tool
- The parting surface with the component area was then created by first trimming away the union of the extrapolated surface and the C surface and then the union of the resulting surface and the B surface using the trim tool
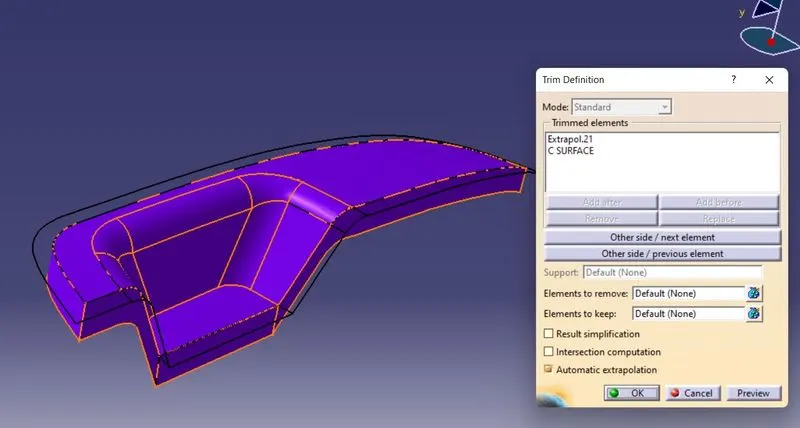
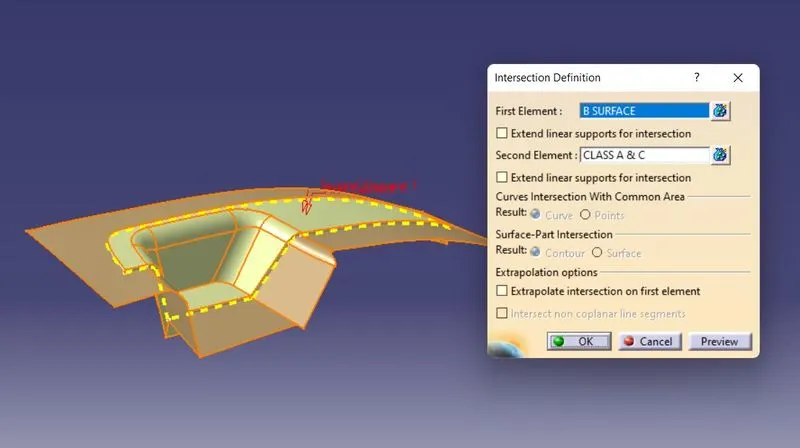
- An intersection of the joint surfaces of Class A and C and the B surface was taken using the intersection tool. This line formed the parting line between the core and the cavity
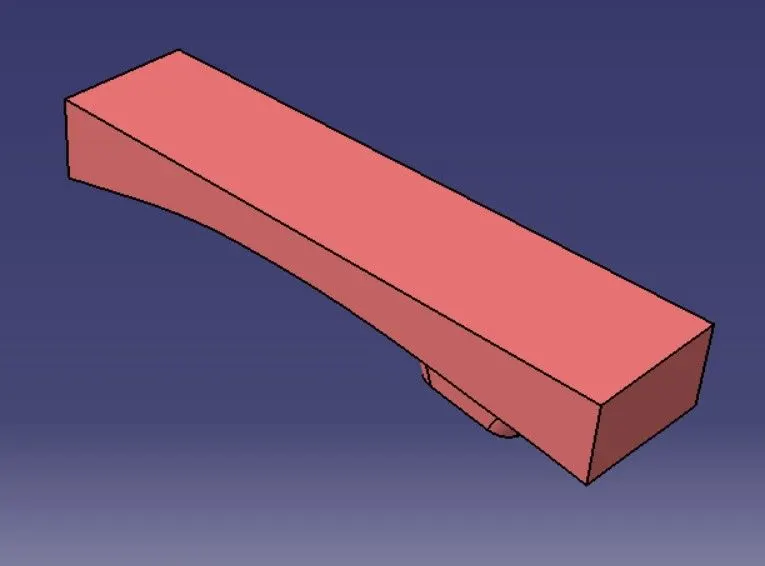
9. Creating the Core Block
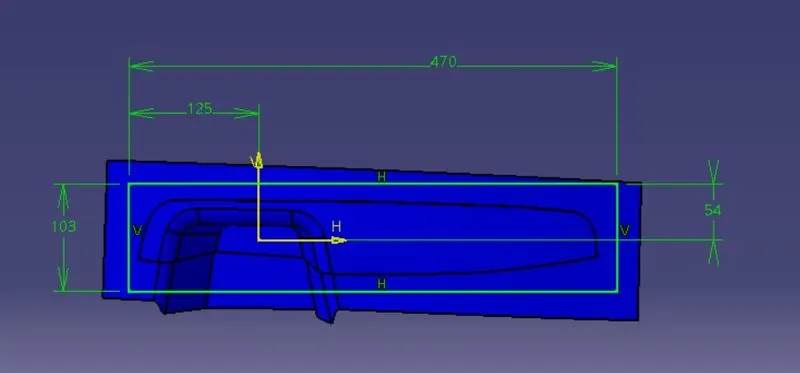
- A rectangular sketch was created in the XY plane which was then extruded using the extrude surface tool to a random height in both the positive and negative Z directions
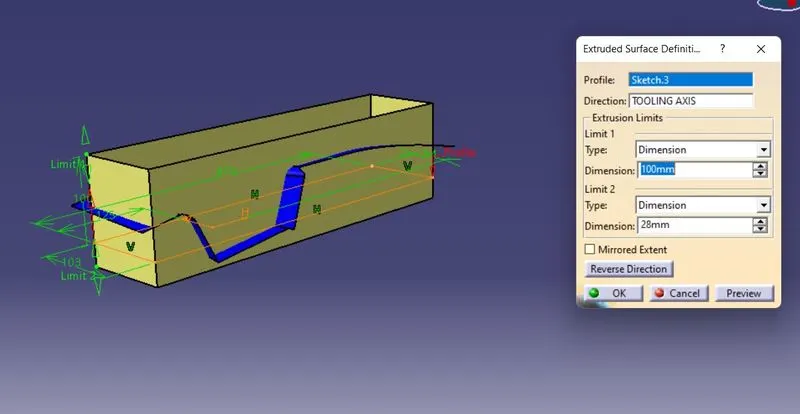
- Using the trim tool, the extruded surface and the parting surface was trimmed to form the surface for the core block
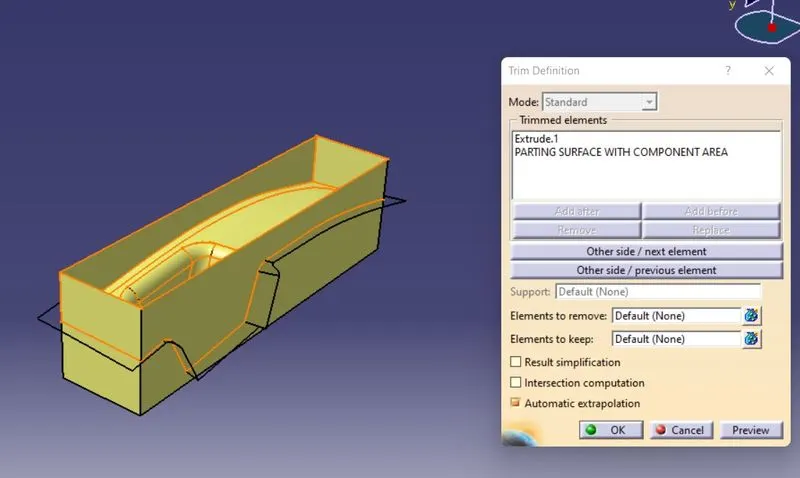
- The top open edges were chosen to close the body using a surface with the help of the fill surface tool
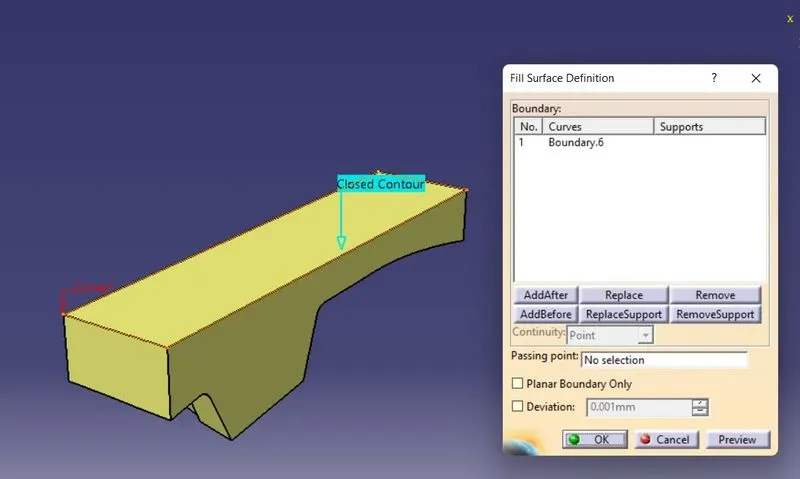
- This surface body was then joined using the join tool and made into a solid body using the close surface tool
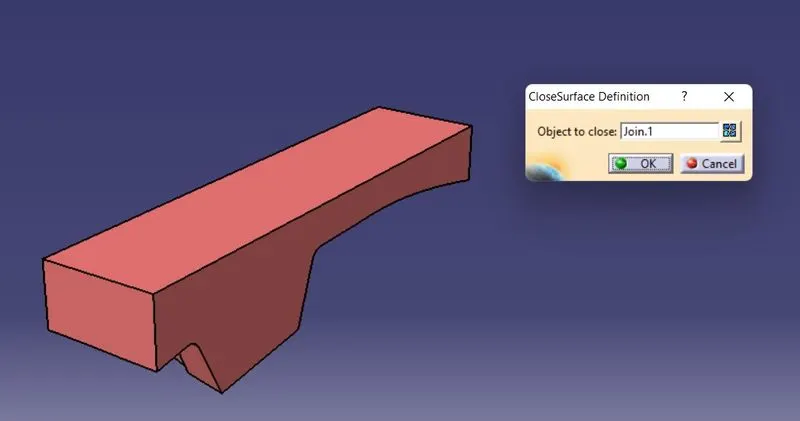
- This final body was the Core Block for the component
10. Creating the Cavity block
- The Cavity Block was created in a similar manner as the Core block except that the trim directions were modified
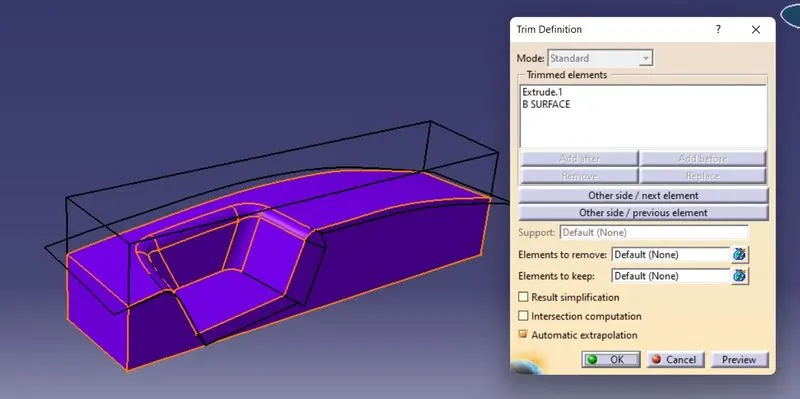
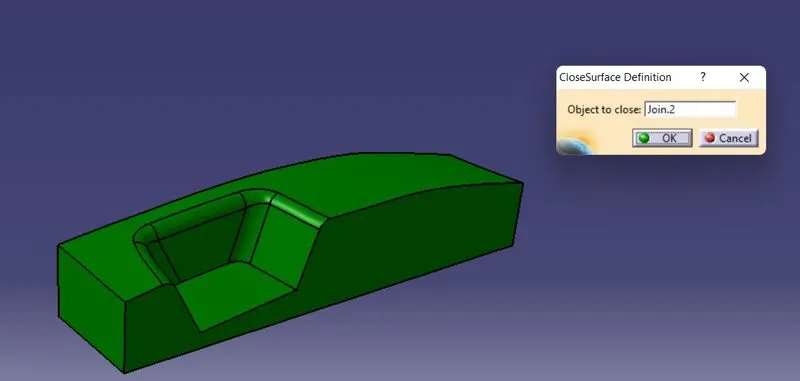
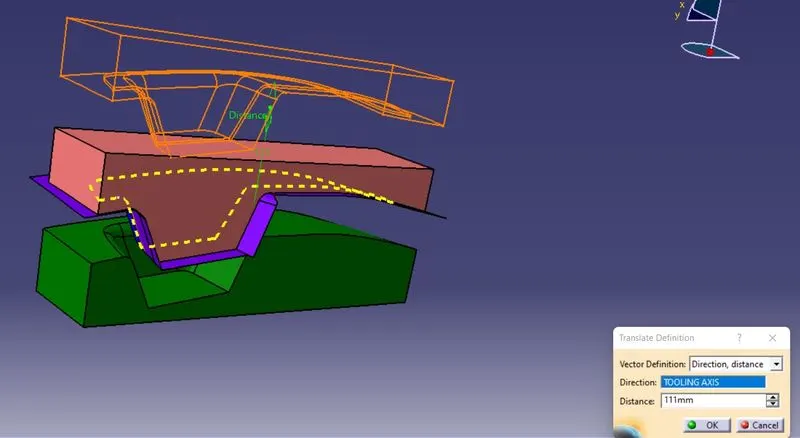
11. Translating the solid bodies to create an understanding of the mold separation process
- The translate tool was used to move the core and cavity blocks along the tooling axis to create a proper understanding of how the mold opens and it was found that the design was manufacturable
11.Publishing the required elements
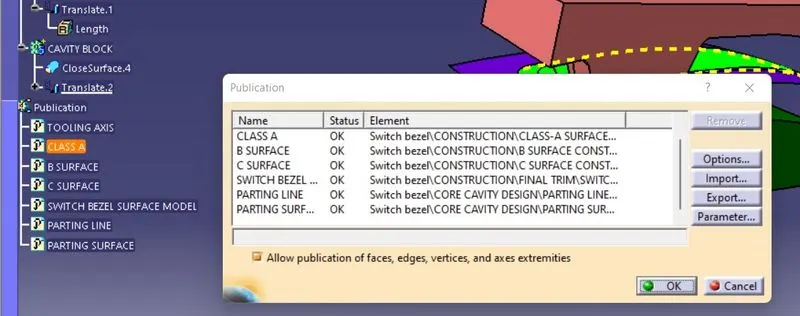
- Publishing geometrical elements makes them available for different users and is important from an assembly context
- In this project, the Class-A, B, C surfaces, the final trim, the tooling axis, the parting line and the parting surface were published
DRAFT ANALYSIS: RESULTS
QUICK ANALYSIS: COLOUR SCALE DISPLAY
CLASS-A SURFACE
SOLID MODEL
ANALYSIS UNDER THE RUNNING POINT
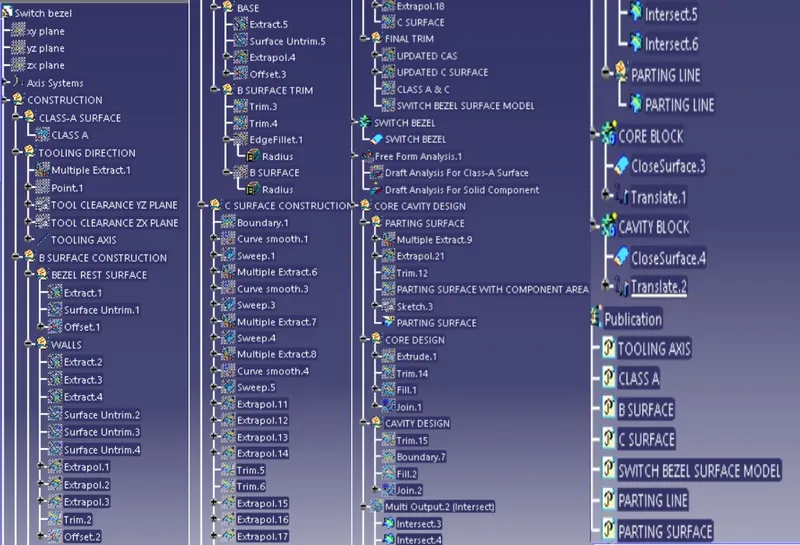
FEATURE TREE
STANDARD VIEWS OF THE MODEL
TOP VIEW
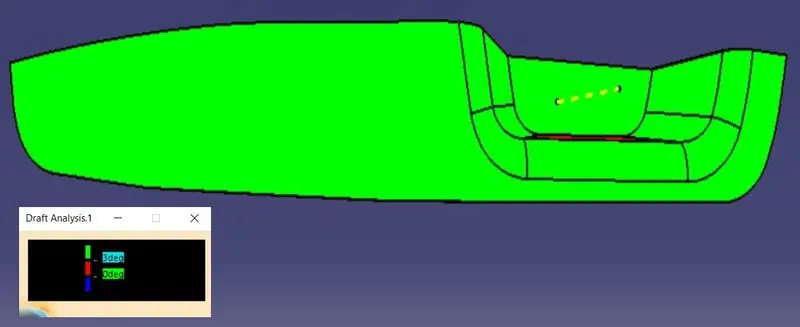
FRONT VIEW
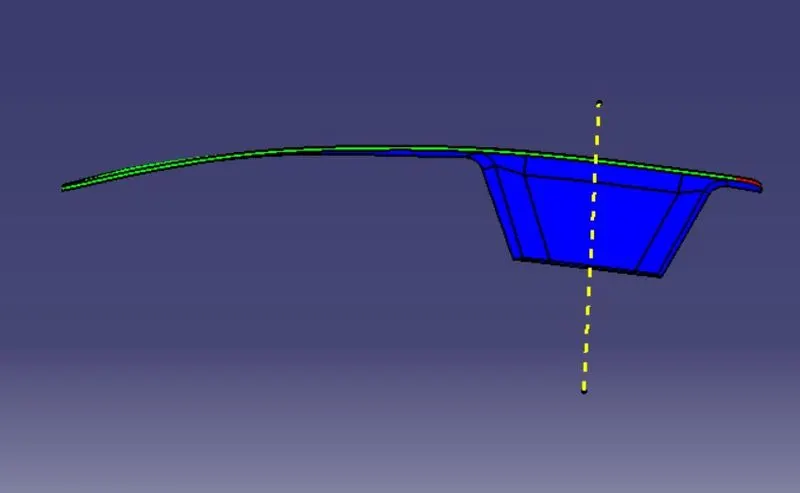
SIDE VIEW (RIGHT)
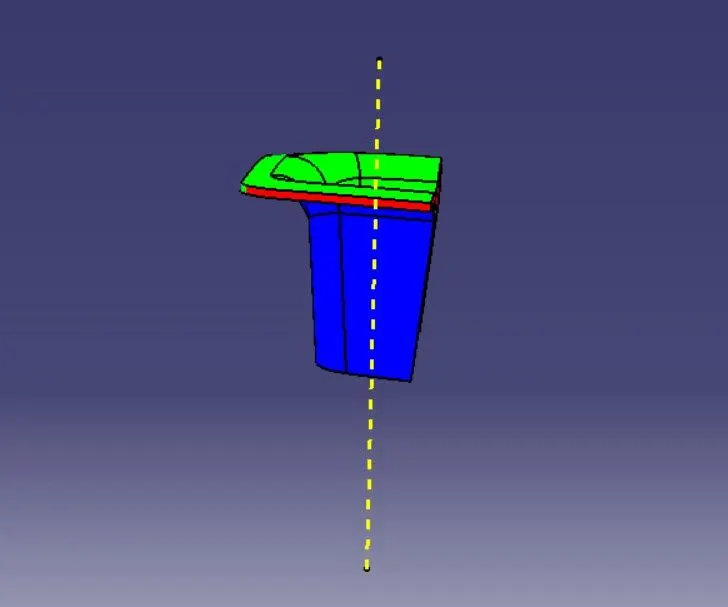
ISOMETRIC VIEW
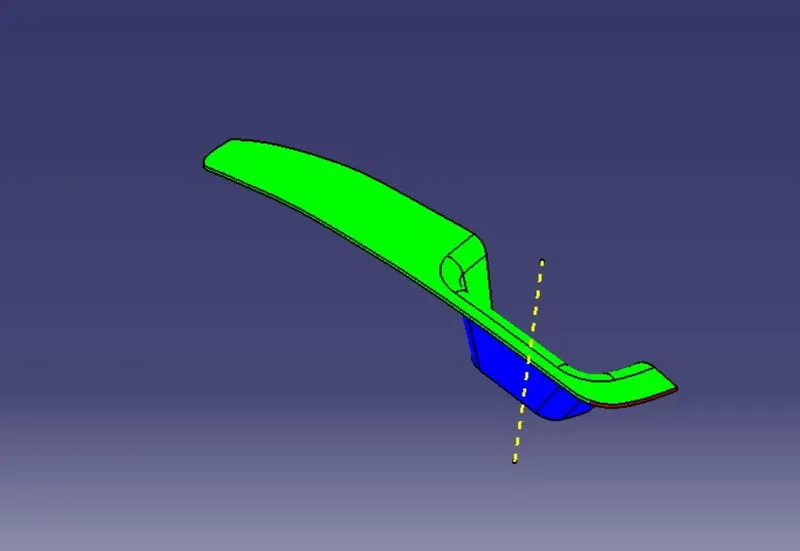
STANDARD VIEWS OF THE CORE BLOCK
FRONT
TOP
SIDE
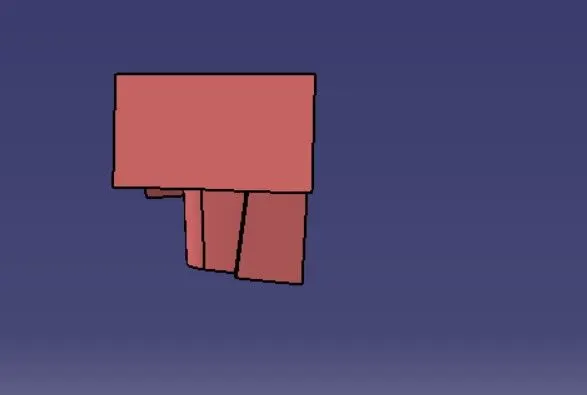
ISOMETRIC
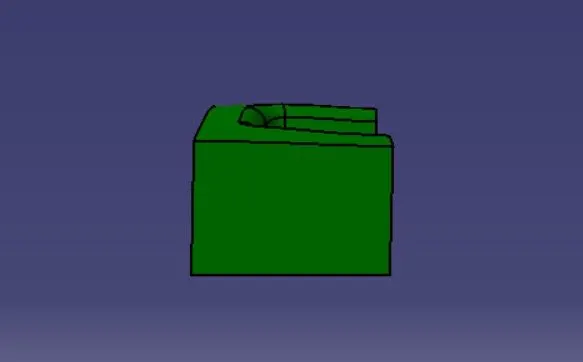
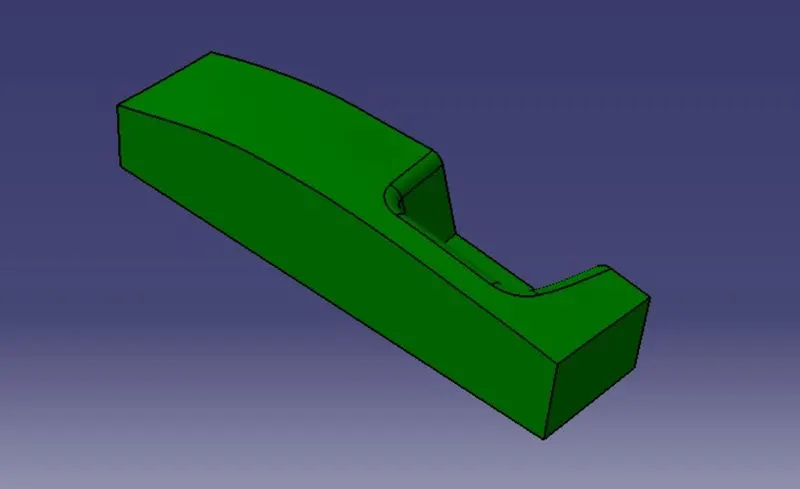
STANDARD VIEWS OF THE CAVITY BLOCK
FRONT
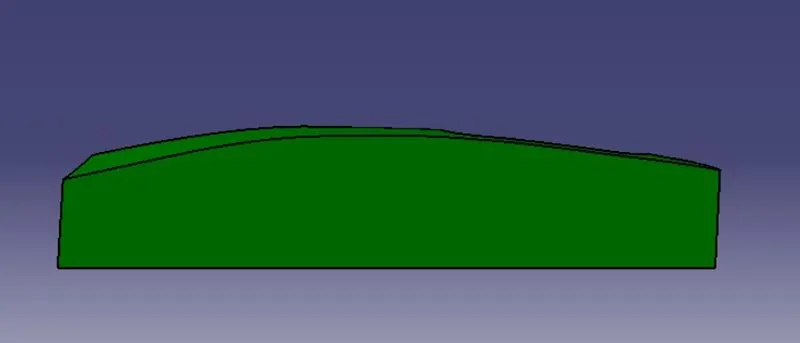
TOP
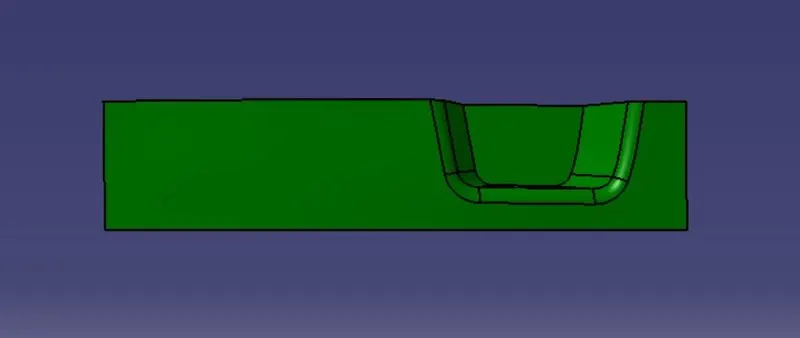
SIDE
ISOMETRIC
CONCLUSION
This project imparted a great deal of knowledge regarding the creation of tooling axis and performing proper draft analysis on a component which are essential steps to ensure a design is fit for manufacture. It also provided valuable insights on the design of a plastic component using Class A, B and C surfaces and the concepts like Core, cavity, parting line and parting surface using CATIA.