(ANSYS_P6) Verification of Weld Joints
WELD JOINT VERIFICATION
INTRODUCTION
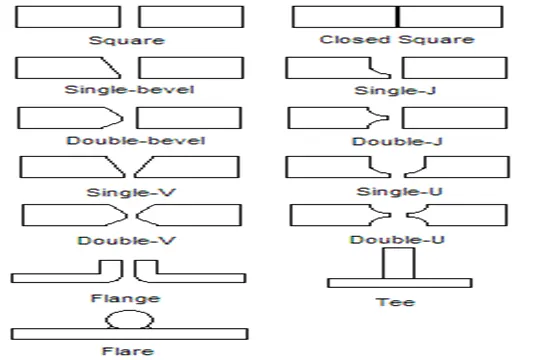
A welding joint is a point or edge where two or more pieces of metal or plastic are joined together. They are formed by welding two or more workpieces (metal or plastic) according to a particular geometry. There are five types of joints referred to by the American Welding Society: butt, corner, edge, lap, and tee. These configurations may have various configurations at the joint where actual welding can occur. There are many types of butt welds, but all fall within one of these categories: single welded butt joints, double welded butt joint, and open or closed butt joints. A single welded butt joint is the name for a joint that has only been welded from one side. A double welded butt joint is created when the weld has been welded from both sides. With double welding, the depths of each weld can vary slightly. A closed weld is a type of joint in which the two pieces that will be joined are touching during the welding process. An open weld is the joint type where the two pieces have a small gap in between them during the welding process.
ANALYSIS
Weld strength verification is analyzed by varying materials between the plates, ribs, and weld materials.
Case_1: Stainless Steel (Plates, ribs, and weldments)
Case_1: Aluminum Alloy (weldments), Stainless Steel (Plates, ribs)
Case_1: Bronze(weldments), Stainless Steel for (plates), Copper (ribs)
GEOMETRY
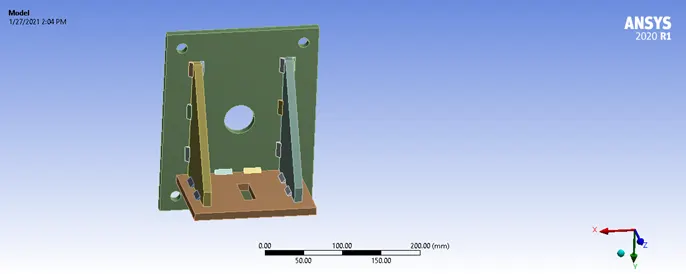
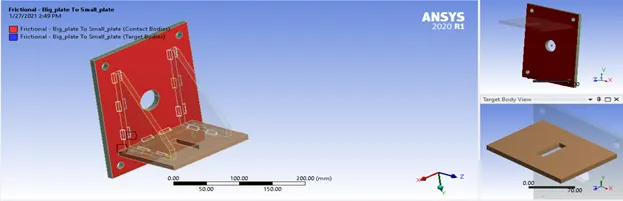
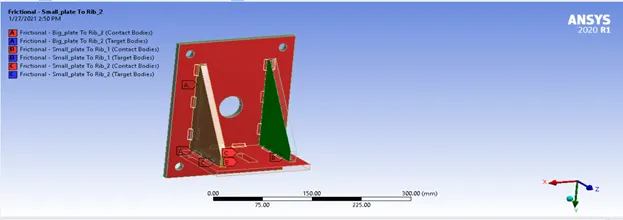
The geometry is imported into space- claim and can be seen below with two plates attached with strength reinforcement ribs by weldments.
MATERIAL AND THEIR PROPERTIES
STAINLESS STEEL
Density: 7750 kg/
Youngs Modulus: 193000 Mpa
Poisson Ratio: 0.31
Tensile Yield Strength: 207 Mpa
Tensile Ultimate Strength: 586 Mpa
ALUMINIUM ALLOY
Density: 2770 kg/
Youngs Modulus: 73800 Mpa
Poisson Ratio: 0.337
Tensile Yield Strength: 363 Mpa
Tensile Ultimate Strength: 449 Mpa
COPPER CAST
Density: 8940 kg/
Youngs Modulus: 125000 Mpa
Poisson Ratio: 0.345
Tensile Yield Strength: 33.5 Mpa
Tensile Ultimate Strength: 152 Mpa
BRONZE CAST
Density: 8810 kg/
Youngs Modulus: 80000 Mpa
Poisson Ratio: 0.345
Tensile Yield Strength: 144 Mpa
Tensile Ultimate Strength: 267 Mpa
MESHING
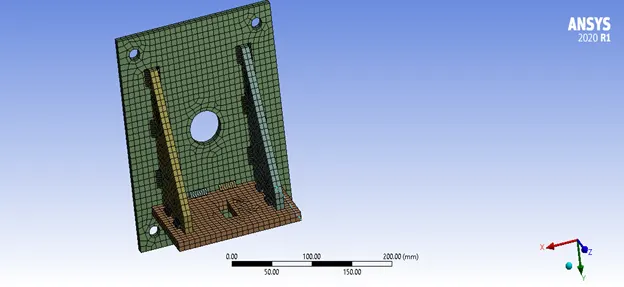
Body Sizing: 7mm (ribs, plates)
Global Element Sizing: Default
PROCEDURE
CONTACT
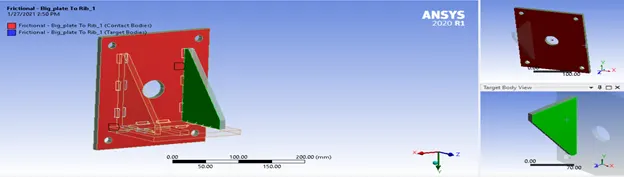
The contacts between the weldments and the plates are specified with bonded type connection. The contacts between the plates and ribs are specified with frictional contact.
BOUNDARY CONNECTIONS
Fixed Supports
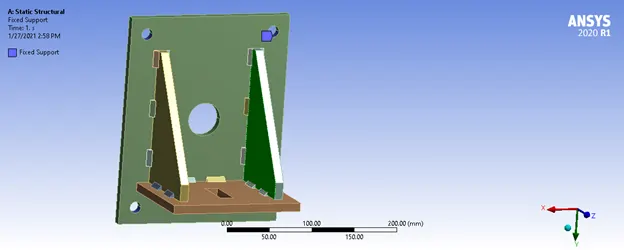
Supports are specified for the four holes to prevent motion in any degree of freedom whatsoever.
Force
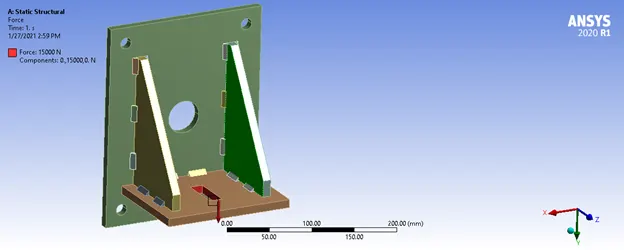
A force of is applied to the faces of the rectangular hole and is specified in the global Y -Axis.
ANALYSIS SETTINGS
Auto Time Stepping: Program Controlled
Solver Type: Program Controlled
SOLUTION
Solution specified is.
- Equivalent Stress of each cases weldment
- Directional deformation of each cases model
- Results is analyzed.
RESULTS
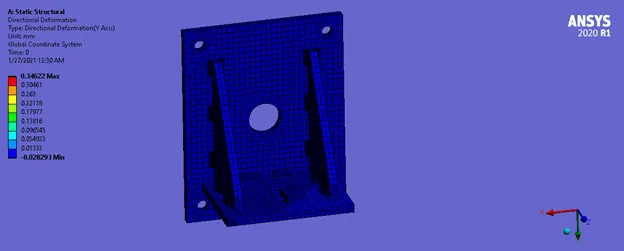
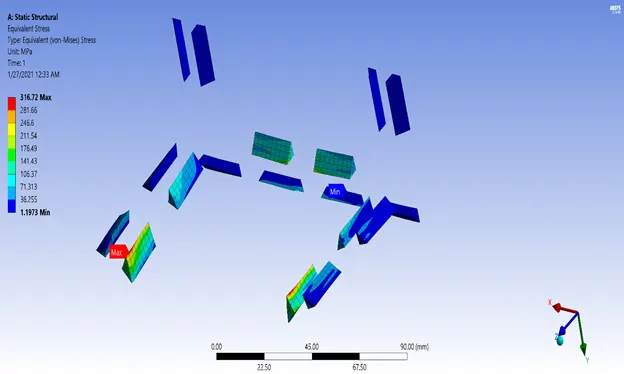
Case_1: Stainless Steel (Plates, ribs, and weldments)
Directional Deformation
Equivalent Stress in the Weldments
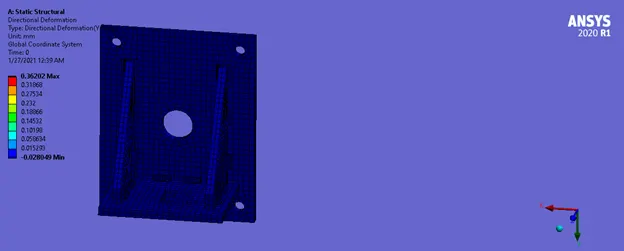
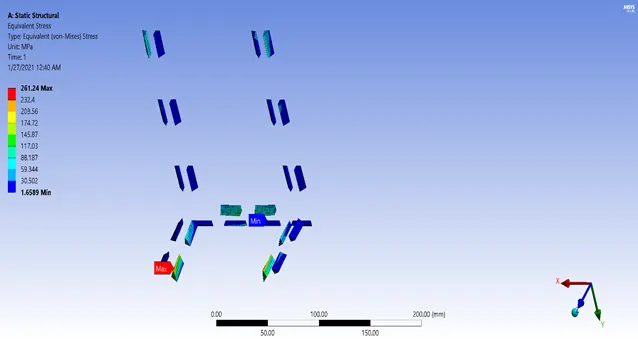
Case_2: Aluminum Alloy (weldments), Stainless Steel (Plates, ribs)
Directional Deformation
Equivalent Stress in the Weldments
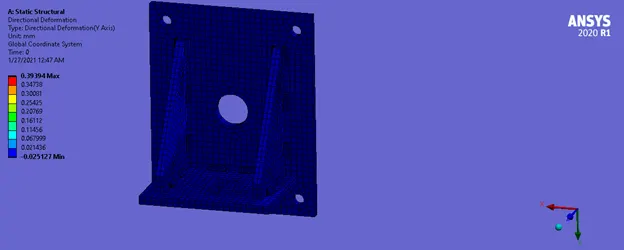
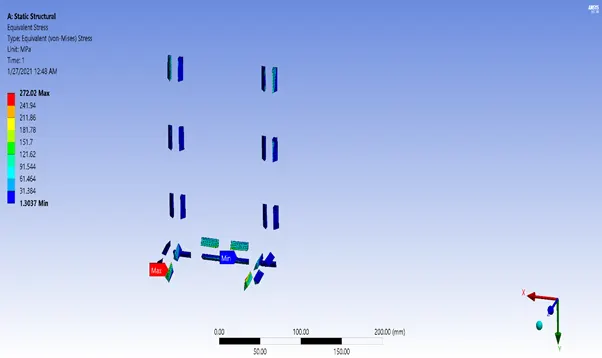
Case_3: Bronze(weldments), Stainless Steel for (plates), Copper (ribs)
Directional Deformation
Equivalent Stress in the Weldments
POST-PROCESSING
|
CASE |
DEFORMATION-Y AXIS (mm) |
EQUIVALENT STRESS (Mpa) |
|
1 |
0.34622 |
316.72 |
|
2 |
0.36202 |
261.24 |
|
3 |
0.39394 |
272.02 |
RESULTS AND DISCUSSIONS
From the results above it can be seen that the maximum deformation is seen in case_3 with plates made from steel and welds from bronze made from stainless steel and the least deformation seen in case_1 with all materials and welds made from stainless steel.
The equivalent stress generated for all the weldments is shown above. The stresses developed on the welds was maximum in the first case. Stresses developed is a resistance to deformation. The case one with structural steel has the highest young modulus, therefore the stiffer the welded joint the lesser the deformation. This explains the weld material having the least deformation and the highest stresses developed compared to the other two cases.
It can also be note that the stresses developed exceeded the tensile strength limit (207Mpa) of structured steel, so the weld material was deformed in the plastic region. But the maximum stress (333Mpa) was less than the ultimate tensile strength of (467Mpa) so no cracking was developed.
Aluminum with a lesser young modulus deformed more than stainless steel and had lesser stresses resistant to the deformation compared to stainless steel.
The bronze weld material had the least strength as it experienced the highest deformation compared to the other three weld materials. With a Modulus of 80000Mpa, it should be stiffer than aluminum which has a modulus of 73000Mpa, but it deformed the most and produced the weakest strength. This is because the ribs of case_2 was made from structural steel as that of case_3 was made from copper. Comparing both copper and steel, steel has higher strength than copper, so it added some more stiffness to the second case as compared to that of the copper which is not stronger than steel.
This variation explains why case_3 developed more stresses in the weld bronze material than that of aluminum weld but deformed more than that of the case _2. The case two weld material is weaker than case three but during deformation of the whole structure, the case_2 is seen to be stiffer than case_3.
CONCLUSION
The difference in material properties used determined how stiff or strong a weld can be. Stainless steel weld material produced the most strength and aluminum weld produced the least stress resistance to deformation.