Week 2:- BiW Fixture Basics Challenge
1. What is the process of project execution activity?
A Project Execution Plan is a governing document that defines how a project is to be executed, monitored, and controlled.
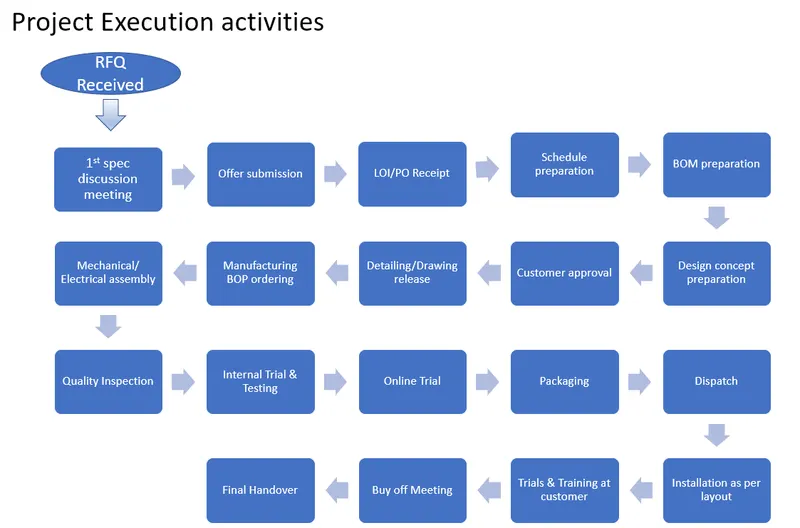
- RFQ received:
For the execution of the project, the first and foremost Data received is a Request for Quotation from the customer. In that, a Basic Details of a required product is mentioned and the deadline of the product is also mentioned.
- Spec Discussion meeting:
this will be the first meeting between the company, other vendors, and customers, where they discuss briefly the RFQ and finalize the given offer and deadlines.
- Offer submission:
the overall finalized offer after some changes of the quotation is submitted to the customer.
- LOI/PO Receipt:
this phase is planned by the customer where a purchase order is done and selecting the material and manufacturing processes. once done by the customer, the company will execute the procedure for the project.
- Schedule Preparation:
This will be the first preparation by the project heads where they schedule and allot time for different processes to the manufacturers.
- BOM preparation:
to manufacture the product, the raw materials, tools, components, standard parts, number of quantities are prepared in the form of bills. (Bill Of Materials)
- Design concept preparation:
to reduce money and time, a Digital image of the product is prepared with the help of CAD systems and software. and make the various concepts of the product.
- Customer Approval:
after making various concepts of the product, the customer will select the satisfying design and approve.
- Details/ Drawing release:
after the selection of the design, then the approved concept is detailed and separated into assemblies and sub-assemblies which will be in the form of 2D Drawing.
- Manufacturing BOP ordering:
Manufacturing of Mechanical/electrical materials and processes are started and purchases of standard parts are done.
- Mechanical/Electrical assembly:
After the manufactured mechanical/electrical parts are inspected and approved, they start to assemble the parts into assemblies or sub-assemblies.
- Quality Inspection:
the parts are taken to various inspection operations until the output is matched according to data.
- Internal trial & testing:
After the successful inspection, the product is taken to trial and tested to check its safety and performance.
- Online Trial:
on the same side, testing of the electric product is done through CAE systems by engineers.
- Packaging:
after the successful trials and testing, the manufacturers and the customer examines the product and get satisfied. then the packaging is started securely.
- Dispatch:
after packaging the product is shipped and dispatched.
- Installation as per layout:
after delivery, the product is installed as per the layout given by the customer.
- Trials & training at the customer:
after installation, the product is tested and at the same time training is given to the customer about the product.
- Buy off meeting:
in this phase, the reviews are taken by the customer and discuss further modifications to the product.
- Final Handover:
after the successful completion, the project details and product is handed over to the customer.
2. What are the types of joining processes?
Joining processes include welding, brazing, soldering, mechanical fastening, and adhesive bonding. Mechanical fastening can be used to provide either temporary or permanent joints, while adhesive bonding, welding, brazing, and soldering processes are mainly used to provide permanent joints.
in joining processes we can choose between mechanical and metallurgical joining based on the material and place of joining.
Mechanical joining: Mostly temporary but some times permanent, which are
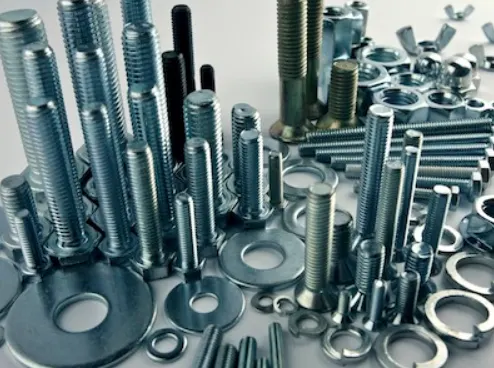
- Mechanical Fasteners
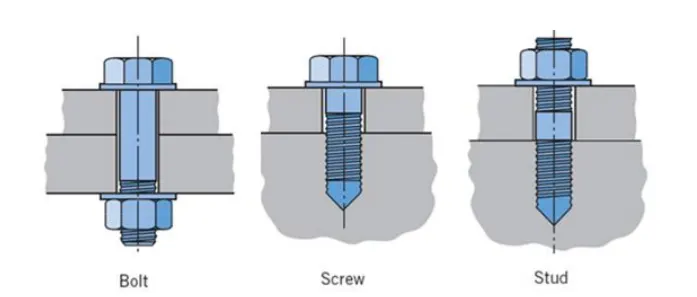
These are temporary joints that are used to fix parts while placing and tightening.
- Rivets
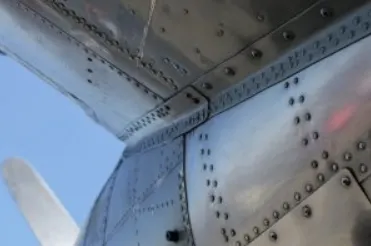
A rivet is a permanent mechanical fastener. Before being installed, a rivet consists of a smooth cylindrical shaft with a head on one end.
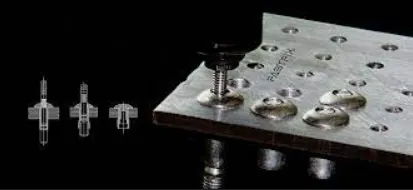
- Hemming
Hemming is a sheet metal forming process in which sheets are joined by bending it usually to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods, and tailgates are formed by the hemming process.
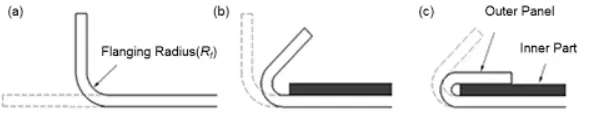
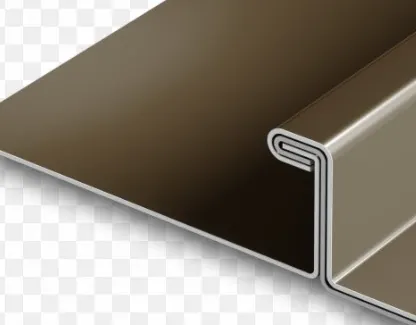
- Adhesive bonds
Adhesive Bonding is the process of joining two surfaces together, usually with the creation of a smooth bond. This may involve the use of glue, epoxy, or one of a wide range of plastic agents that bond either through the evaporation of a solvent or through curing via heat, time, or pressure.
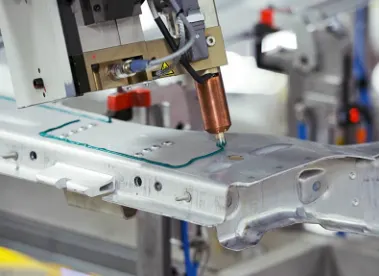
Metallurgical joining: only permanent joining processes.
- Welding
It is an economical way to join components in terms of material usage and fabrication costs. Other methods of assembly require, for example, drilling of holes and usage of rivets or bolts which will produce a heavier structure.
there are many types of welding
- Arc Welding
Arc welding is a type of welding process using an electric arc to create heat to melt and join metals
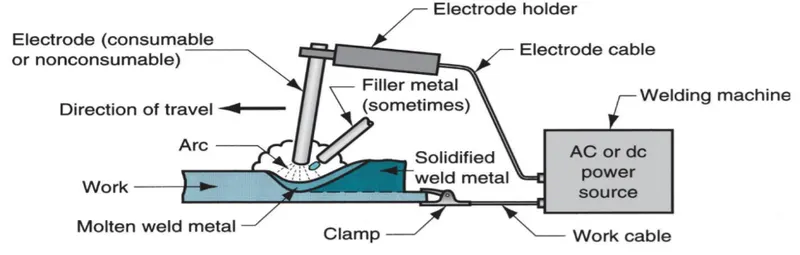
types of arc welding
- Gas tungsten arc welding
- Gas metal arc welding
- plasma arc welding
- Resistance welding
Resistance welding is the joining of metals by applying pressure and passing current for a length of time through the metal area which is to be joined.
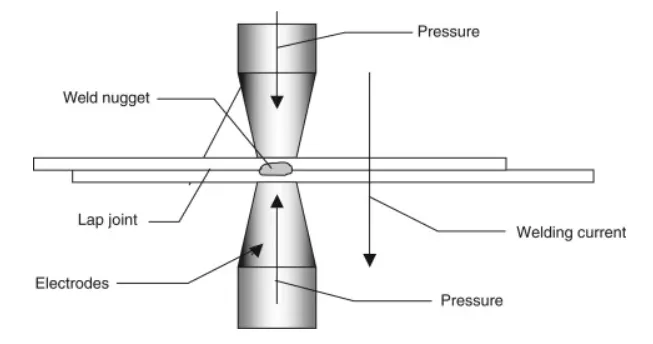
types of resistance welding
- Spot welding
- Seam welding
- projection welding
- Resistance butt welding
- Gas welding
Gas welding involves the melting of base metal and filler metal is used, through the flame produced at the tip of a welding torch.
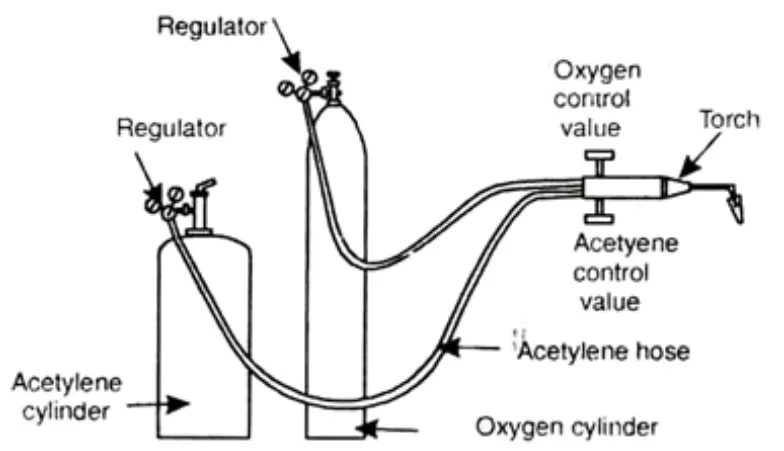
types of gas welding
- oxy-acetylene gas weld
- oxyhydrogen gas weld
- air- acetylene gas weld
- pressure gas weld
- Thermochemical welding
Thermit welding is a chemical welding process in which an exothermic chemical reaction is used to supply the essential heat energy.
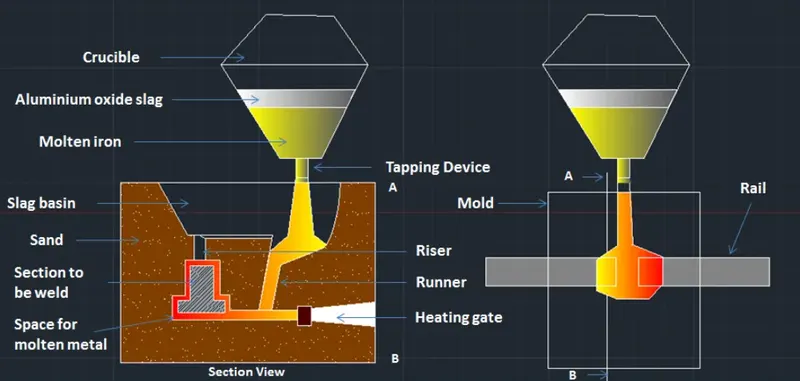
types of thermochemical welding
- thermit welding
- atomic hydrogen welding
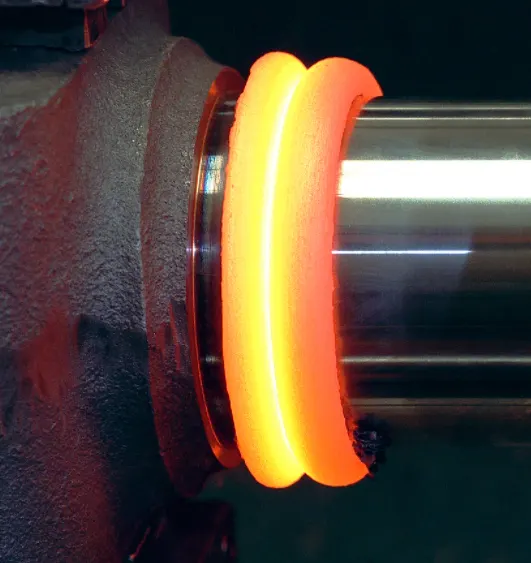
- Friction welding
Friction welding (FRW) is a solid-state welding process that generates heat through mechanical friction between workpieces in relative motion to one another
- Brazing
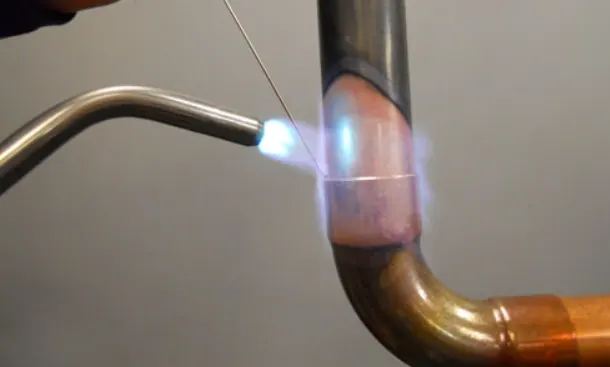
Brazing is a metal-joining process in which two or more metal items are joined together by melting and flowing a filler metal into the joint, with the filler metal having a lower melting point than the adjoining metal. Brazing differs from welding in that it does not involve melting the workpieces.
- Soldering
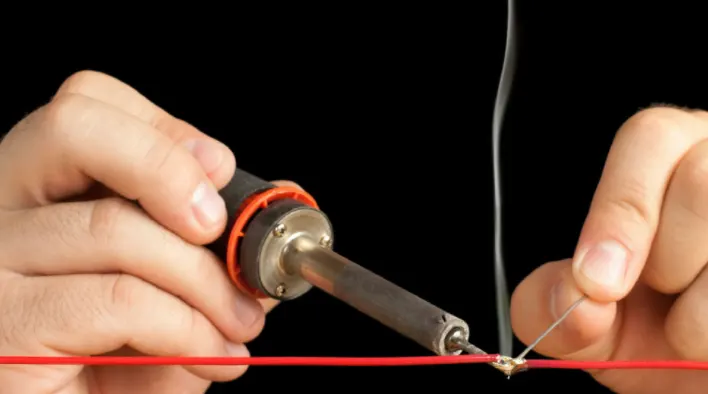
soldering is a joining process used to join different types of metals together by melting solder. Solder is a metal alloy usually made of tin and lead which is melted using a hot iron. The iron is heated to temperatures above 600 degrees Fahrenheit which then cools to create a strong electrical bond.
3. What is Resistance Welding & its application in the automotive sector?
Resistance welding is the process in which two or more parts are welded by the coordinated and regulated use of heat and pressure. The heat in the resistance welding process is generated by the resistance offered by the workpieces to the flow of low voltage high-density electric current. The resistance welding processes include spot welding, seam welding, roll spot welding, projection welding, upset welding, flash welding,,, and percussion welding.
- Resistance spot welding
In this process, the fusion of electrodes is done by electrodes having opposing charges at one location. The sheet thickness has to be less than 3 mm for a good spot weld.
- Seam welding
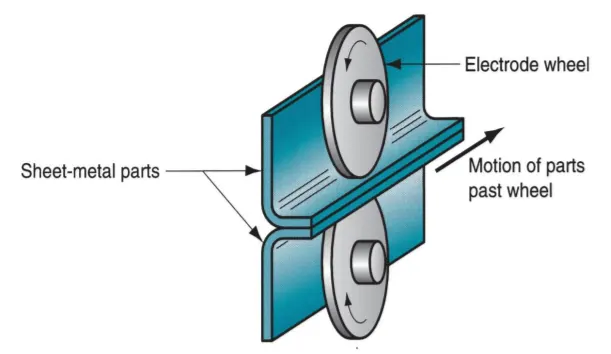
In principle, seam welding is similar to spot welding except that it uses disc-shaped electrodes. Unlike spot welding,,, the disc-shaped electrodes are not separated after each weld but maintain a continuous pressure over the workpieces.
- Flash welding
Flash welding is a type of resistance welding that does not use any filler metals. The pieces of metal to be welded are set apart at a predetermined distance based on material thickness, material composition, and desired properties of the finished weld.
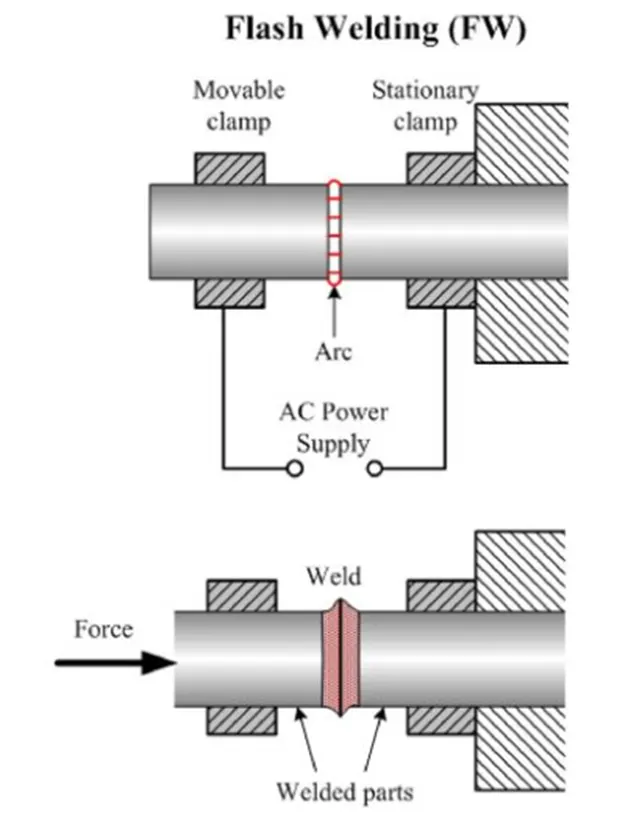
Its applications in the automotive sector are
Resistance Spot Welding (often just called spot welding) is a cost-effective joining technology that continues to be very popular in the automotive industry where high reproducibility and automation are essential criteria. resistance spot welding has proven itself as the dominant technology when joining thin metal sheets.
In particular, the automotive industry continues to use resistance spot welding as its main joining process, despite strong competition from the processes of beam welding, adhesive bonding,,, and mechanical joining. The main reason for this are that resistance spot welding offers high productivity at a low cost and is therefore, likely to maintain its position into the future.
- Resistance welding is used in mass production for welding sheet metal, wire,and tubes.
- It is used in welding bars, boxes, cans, rods, pipes, and frames metals of medium and high resistance materials such as steel, stainless steel, money metal, and silicon bronze which are easy to weld.
- It is used for making fuel tanks for cars, tractors, etc.
4. What is fusion welding & types of fusion welding with their application in the automotive sector?
In fusion-welding processes, heat is applied to melt the base metals. In many fusion welding processes, a filler metal is added to the molten pool during welding to facilitate the process and provide strength to the welded joint. When no filler metal is used, that fusion welding operation is referred to as Autogenous weld. Types: Arc welding, Resistance welding, Gas welding, electron beam welding, laser welding
Arc Welding
Arc welding is a type of welding process using an electric arc to create heat to melt and join metals
Applications of arc welding
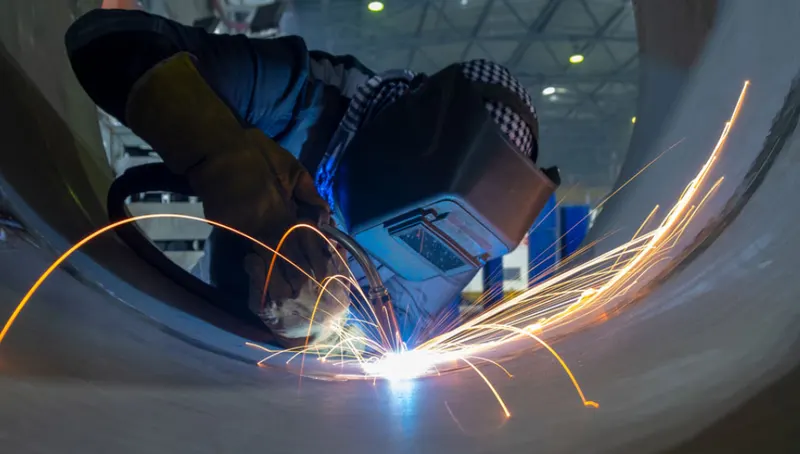
-Used in the weldings of sheet metals
-For welding thin, ferrous & non-ferrous metals
-The developments of piping in industries
-These weldings are used for repairing dies, tools, and mostly on metals that are made with magnesium & aluminum.
-Used to weld small-diameter parts, thin wall tubing, making it applicable in bicycle industries
Resistance welding
Resistance welding is the joining of metals by applying pressure and passing current for a length of time through the metal area which is to be joined.
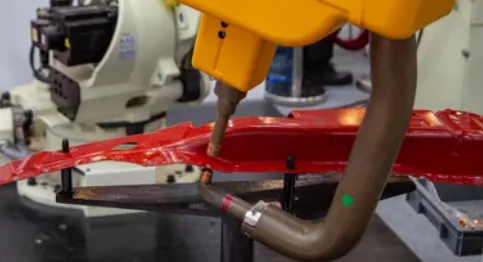
Applications of Resistance welding
Resistance welding is used in mass production for welding sheet metal, wire, and tubes.
- It is used in welding bars, boxes, cans, rods, pipes, and frames metals of medium and high resistance materials such as steel, stainless steel, money metal, and silicon bronze which are easy to weld.
- It is used for making fuel tanks for cars, tractors, etc.
Gas welding
Gas welding involves the melting of base metal and filler metal is used, through the flame produced at the tip of a welding torch.
applications os gas welding
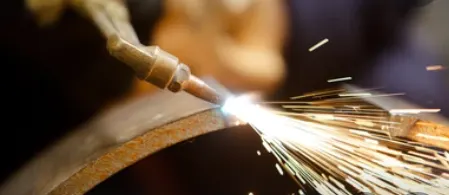
The most commonly used welding methods for automotive applications are resistance spot welding, resistance seam welding, metal inert gas (GMAW) welding, tungsten inert gas (GTAW) welding as also laser beam welding (LBW), friction welding (FW), and plasma arc welding (PAW).
-MIG and TIG welding as cost-effective with high gap bridging capability have successfully been used to obtain Aluminium and magnesium alloy joints with satisfactory properties.
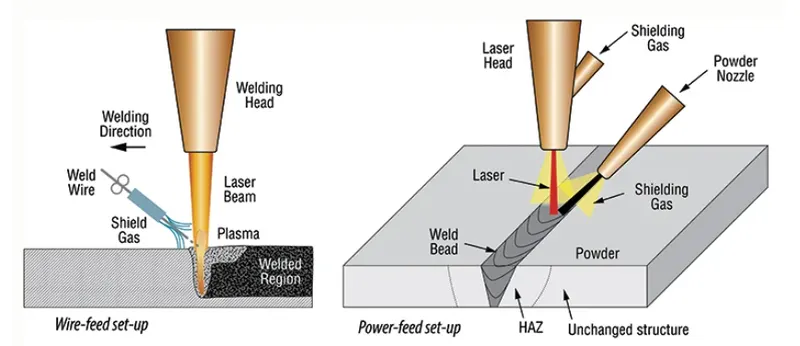
Laser Beam welding
Laser welding utilizes a laser beam as a concentrated heat source to join multiple pieces together. Delivering a focused heat source, laser welding creates a strong seam at a high speed.
The processes and applications of laser welding are most prominent in the automotive industry, where lasers boost productivity at a low cost when welding automotive parts – such as roof, door, or filter assemblies – together.
5. What is the 3-2-1 principle?
It is also known as a six-pin or six-point location principle. In this, the three adjacent locating surfaces of the blank (workpiece) are resting against 3, 2, and 1 pin respectively, which prevent 9 degrees of freedom.
The 3-2-1 principle is a Component holding principle where three pins are located on the 1st principle plane, i.e. either XY, YZ, ZX. And two pins are located on the 2nd plane which is perpendicular to the 1st plane, and at last one pin on the plane which is mutually perpendicular to the 1st and 2nd planes. By using this method Component can be arrested in all six degrees of freedom.
to follow this principle, one has to completely arrest all DOF of a given part.
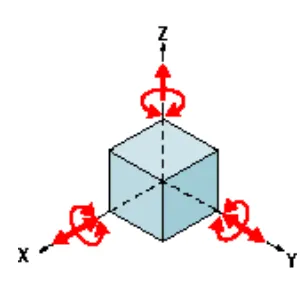
Translational & rotational position along the X-axis
Translational & rotational position along the Y-axis
Translational & rotational position along the Z-axis
These six coordinates are known as the six degrees of freedom of a three-dimensional object. The translational and rotational positions can vary in either direction concerning each of the three axes.
To completely prevent movement, all six degrees of freedom must be restricted.
So, to arrest each DOF Fixtures are used to contain the part for working.
6. Define Body coordinate system?
In geometry, a coordinate system is a system that uses one or more numbers, or coordinates, to uniquely determine the position of the points or other geometric elements on a manifold such as Euclidean space. The order of the coordinates is significant, and they are sometimes identified by their position in an ordered tuple and sometimes by a letter, as in "the x-coordinate".
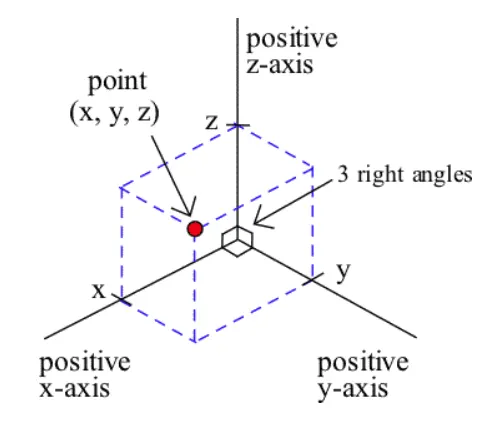
In-Vehicle body coordinate system. the (XYZ) coordinates are defined as,
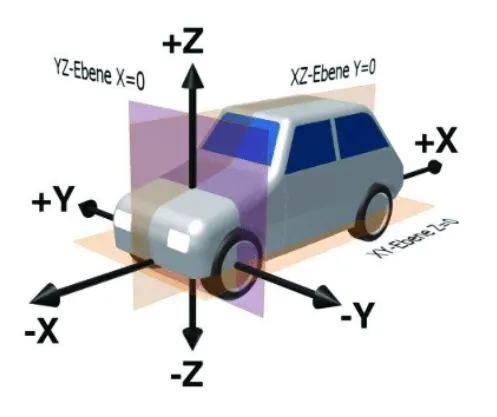
A coordinate system is used for the positioning of the points, lines, or even parts as in the design perspective.
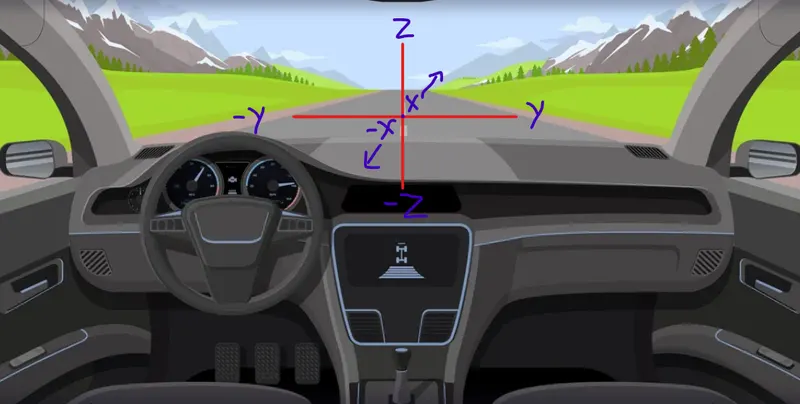
if we take an example from the driver's point of view, we can understand the coordinate system more easily
- A driver's front and back view from the vehicle is called ( X and - Xaxis). In automotive industries, these x coordinates are mentioned as " car forward and Car Rearward".
- A driver's left and right side view from the vehicle is called ( Y and - Y-axis). in automotive industries, these Y coordinates are mentioned as" car outboard and car inboard".
- A driver's top and bottom side view from the vehicle is called ( Z and - Zaxis).
7. Elaborate Body plane system & its essentials.
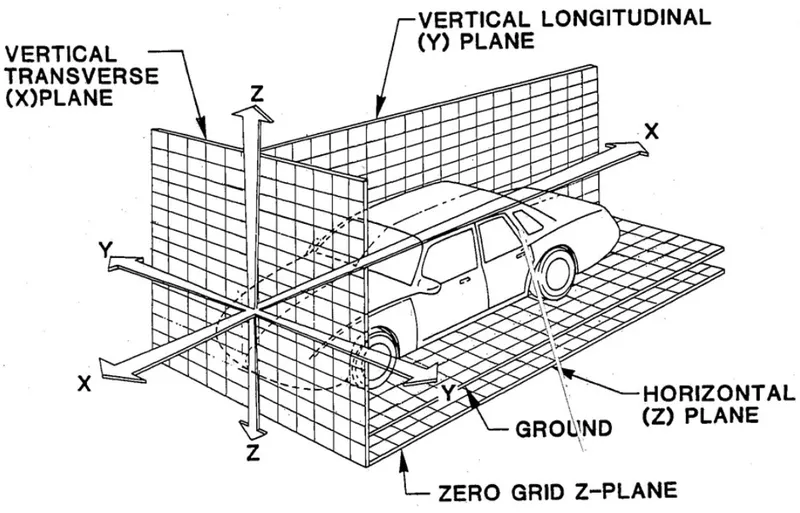
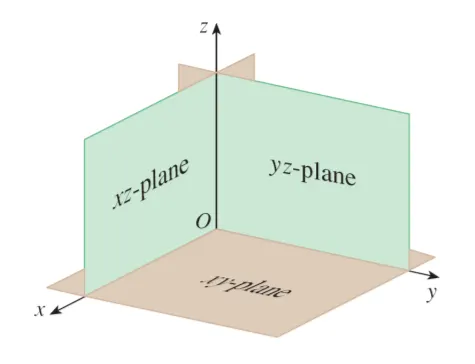
A plane system is used to create the points or lines on a particular view or surface.
The essentials of plane system is,
- By using plane system we can maintain standards within country.
- by using plane system for creation of single parts, the assembling is easier.
- by coordinate plane system we can identify the points or parts location quickly.