Project 1 Mechanical design of battery pack
Q: Battery pack capacity: 18 kWh
Cell: ANR26650M1-B
Prepare a detailed battery pack drawing along with its enclosure. State your assumptions.
Ans:
Objective:
To create a battery pack drawing of 18KWh using series and parallel connectios of battery modules made up of individual Li-ion cells.
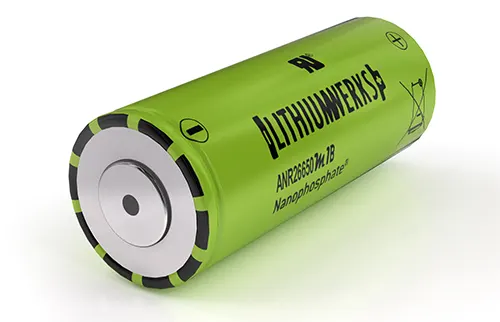
Li-ion cell used hear is of model ANR26650M1-B from the manufacturer of Lithiumwerks.
To discuss about the enclosure used for battery pack.
Li-ion cell(ANR26650M1-B):
This Li-ion cell is manufactured by Lithiumwerks.They deliver very high power due to their use of patented Nanophosphate battery technology.
Based on the Lithium iron phosphate chemistry(LiFePO4),the cells are inherently safe over a wide range of temperature and conditions.
For outstanding cycle life,stable float reliability this cells are suitable for a wide varity of power,pulse and stand by applications.
Nanophosphate battery technology offers thermal stable chemistry,fast charging,consistent output,low capacity loss over time.
It provides extremely safe conditions for while meeting most demanding customers requirements.Multiple layers of protections are employed on chemistry,cell and system
level to acheive an energy storage solution with superior safety.
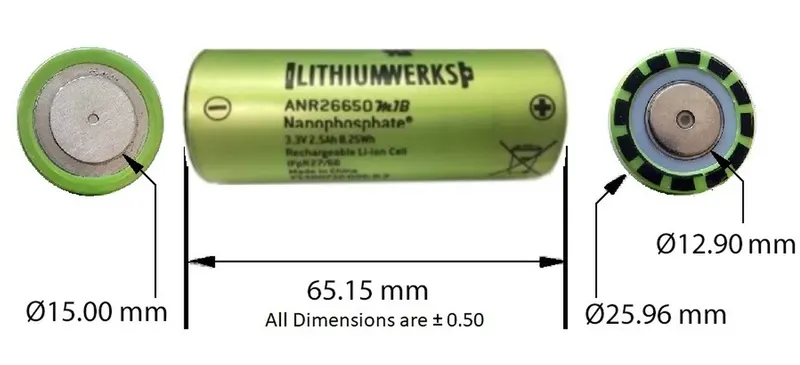
Dimensions:
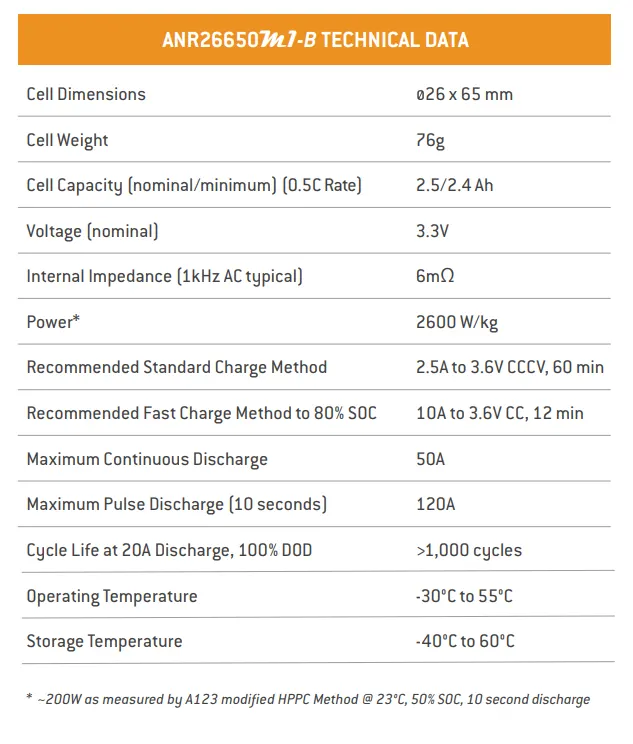
Cell specifications:
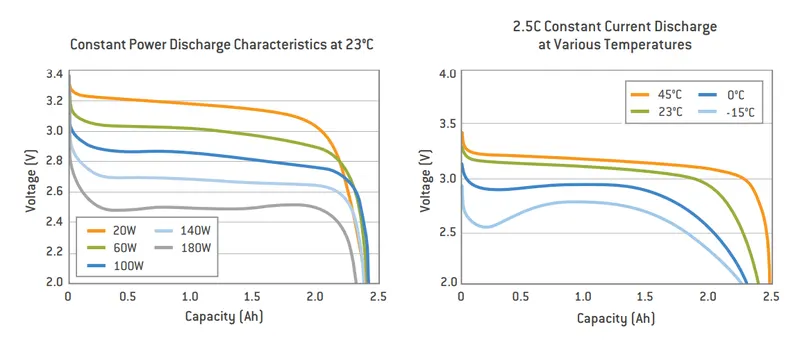
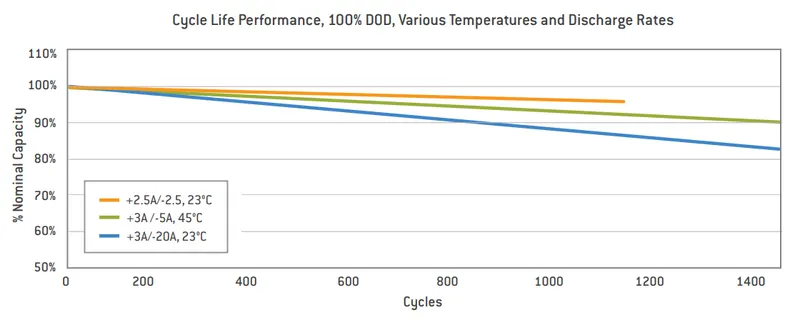
Discharge voltage profile and cycle life with respect to different operating temperature from data sheet:
Assumptions:
We are assuming the overall voltage required to operate the motor and other acessories of electric vehicle as 72V.
So we have constructed the battery pack of 18KWh for a 72 V input voltage motor.
Construction of battery pack:
To construct a battery pack initially we have to estimate the voltage requirement of the overall load of vehicle.
We had assumed as 72V as mentioned above.
Then the battery modules should be created in such a way that the overall voltage is matched with the load requirement voltage.
The modules can be created in series/parallel connections of individual cells. Then every module should be connected in series/parallel to construct the final battery pack.
In series connecction-Voltage added and Current remains same.
In Parallel connection-Voltage remains the same and Current gets added.
Here in our case single cell voltage is 3.3V and a capacity of 2.56Ah. The energy provided from single cell is given 8.25Wh.
So, for the 18KWh battery pack, we need approximately(18000/8.25=2182 cells).
We have to create a single module to produce 72V for our load requirement.
So to obtain 72 V output, cells are connected in series where voltage becomes added and current remains the same.
To obtain 72V ,no of cells required is approximately 22 cells required.(72/3.3=21.8 cells).
Thus single module gives 72V from 22 cells but energy of one module is not enough to run the vehicle as motor power rating is higher.The energy generated from
single module is (22*8.25Wh=181.5Wh).
So to construct a battery pack with 18KWh with not exceeding 72V the modules are connected in parallel.In this parallel connections the currents are getting added and voltage remains same as 72V. As current increases the power of battery pack increase to run the motor load of high power rating.
Now we have to find how many similar modules should be connected in parallel to acheive 18KWh battery pack.
This can be calculated as (18KWh/181.5 Wh =99.17), which gives as nearly 100 similar modules should be connected in pararallel to acheive 18KWh battery pack.
Thus the battery model is said to be a 22S100P configuration(22 series and 100 parallel connections), which gives us (22*100 =2200 cells). From this, we have created the overall capacity of the battery pack as (2196*8.25Wh=18117Wh) which is slightly higher than 18KWh.
The overall Capacity(Ah) of battery pack is given as (2.5Ah * 100 = 250Ah).
Which means it provided 250 A of current continuously for one hour to full discharge.
Thus 100 modules should be arranged in a way as a battery pack to fit in an EV chasis.
Enclosure construction:
To find overall enclosure volume we have to find the volume of single module volume consisting of 22 cells in series connection and multiplied with 10 parallel connected module volume.
ANR26650 cell has 26mm diameter and 65mm height. On the basis of that we need to decide battery size of battery casing.
Length of casing (L) = number of cells at series*(cell diameter (26) + margin at both side of cell (4)) + clearance at the side(2(cell dia + margin)).
L= 22*(26+4)+60
L= 720mm
Breadth of casing (B) = number of cells at parallel*(cell diameter (26) + margin at both side of cell (4) + Clearance at side(2(cell dia + margin)).
B= 100*(26+4)+60
B= 3060mm
Height of casing (H) = 65+35 (Height of cell + margin for wiring ,Cell holders and metal strips)
H = 100 mm
Weight of battery pack
Cell weight = 76g
Number of the cells = 2182
Battery pack weight (W) = cell weight*number of cells + weight of accessories
W = 76*2182 + 4.5 = 165.8 + 4.5 = 170.3 kg
Materials and process in battery pack construction:
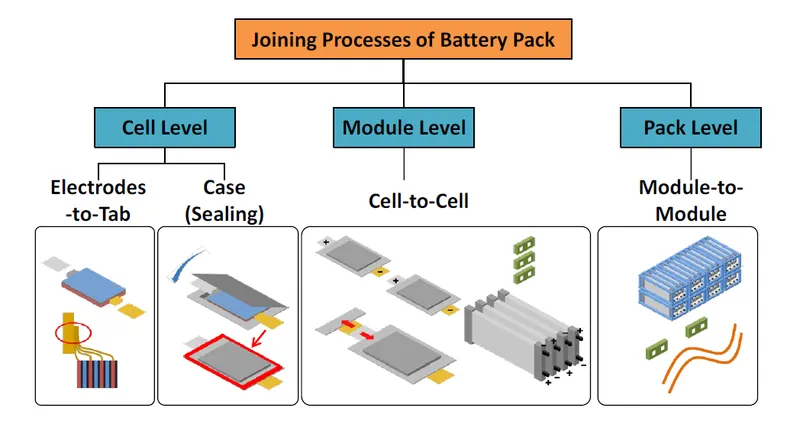
Battery pack constructions consist of three major levels of processings namely cell level,module level,pack level constructions.
The electrodes are combined with electrolyte to various cell models as cylindrical,prismatic,pouch type cells.
After case sealing cells are combained to form module level construction.Finally these modules are combained to form pack level constructions.
Joining technologies of cells:
The interconnections between cells/modules are practised by various welding techniques.Some of them are,
- Ultrasonic metal welding.
- Resistance welding.
- Laser beam welding.
- Wire bonding.
- Mechanical Jooining.
Ultrasonic metal welding-
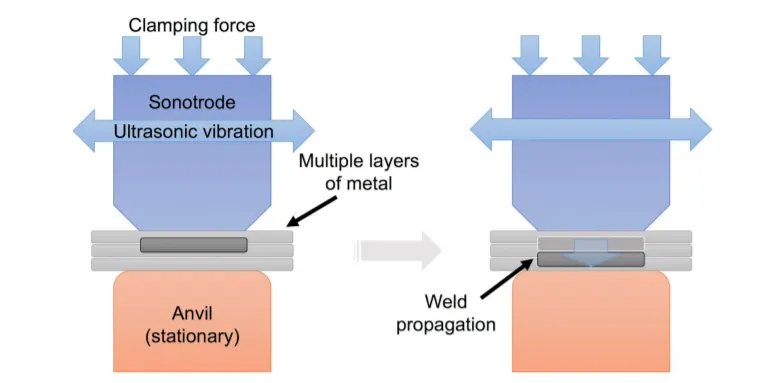
Ultrasonic metal welding or UMW, is a solid-state welding technique which forms a bond by applying moderate static pressure and an ultrasonic oscillation of about 20 kHz between two
parts of metal. The solid-state weld is formed through the high frequencymotion between the parts causing continuous shearing and plastic deformation, while also removing any oxide layers
or contaminants.
Most metals can be ultrasonically welded and the method is excellent for welding together thin foils, as well as thicker sheets with spot or seam welds and also wires.
The four types of materials welded in this process can be seen as,
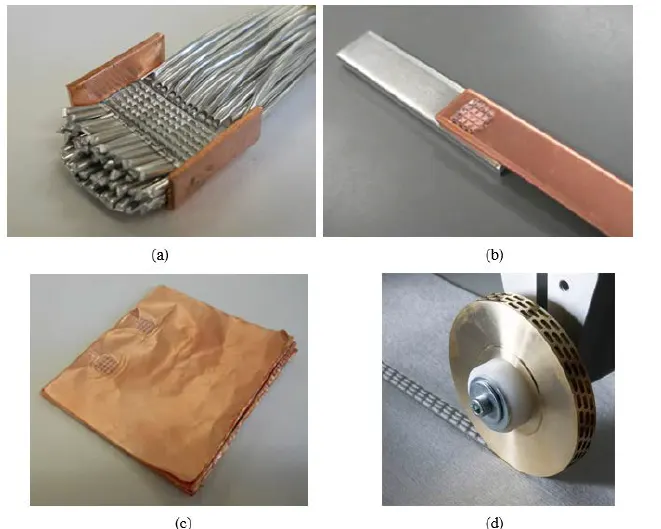
a)Aluminium wire welding on copper.
b)Copper and aluminium welding.
c)Multilayered copper foil welding.
d)Ultrasonic seam welding.
Resistance spot welding-
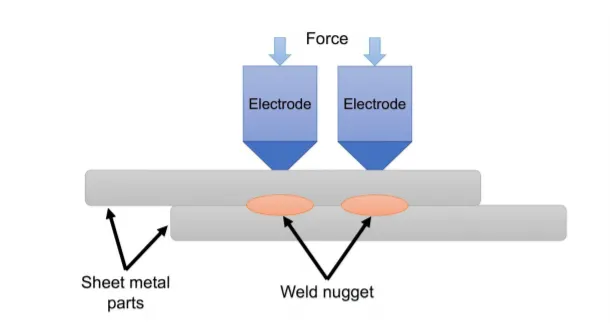
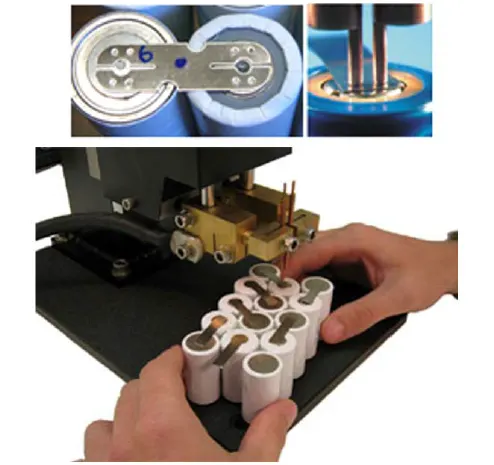
One of the oldest welding methods is resistance spot welding (RSW).RSW is a technique where two or more metal sheets are welded together through the application of an electrical current
and pressure between two electrodes. The electrical resistance of the material at the interface results in the generation of heat and melts the materials together without the use of
filler material or gases.
The temperature increases in the affected area, the interface, and eventually reaches the material’s melting point. A weld nugget forms in the affected area after cooling.
This is a small volume of the material which has melted and then fused together.
Laser beam welding-
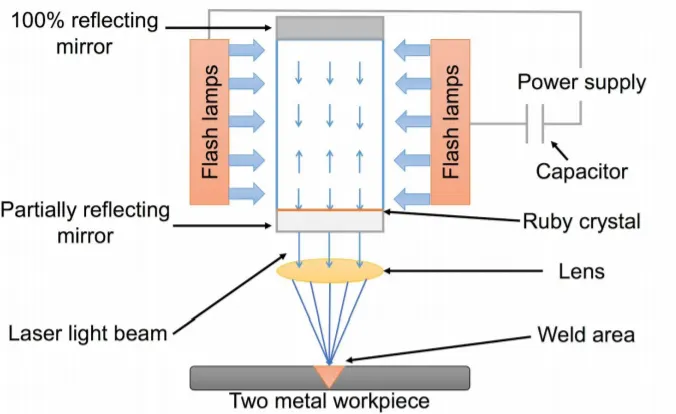
Laser beam welding or LBW is a welding technique in which a laser beam provides a concentrated heat source that fuses the materials together.
LBW is commonly performed using keyhole mode welding in which the extreme power density of the laser beam causes the metal to melt and evaporate.
As the metal atoms evaporate from the surface, forces in the opposite direction of the evaporation causes a local vapor pressure. The vapor pressure creates a hole which is known as the
keyhole by depressing the molten metal.
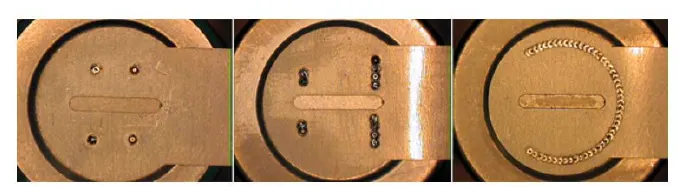
Here below shown the welding of busbars to cylindrical battry cans.
Enclosures:
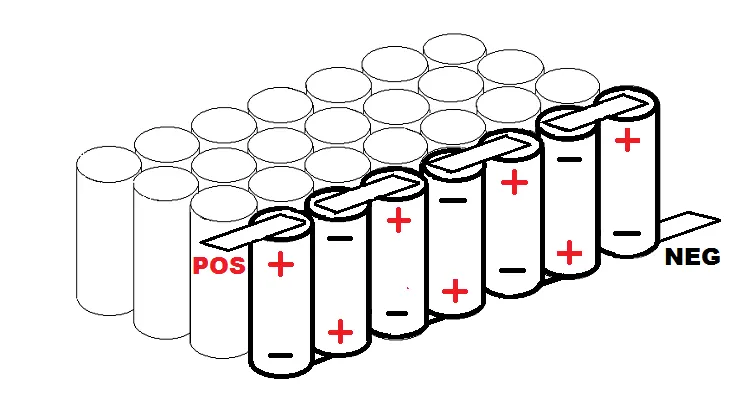
Cells in series connection-
When you connect cells together in series, it doesn’t change the amps or the capacity, it only raises the voltage of the pack. Hooking them up in series means that you connect the positive end
of one cell (or P-group) to the negative end of the other as shown below.
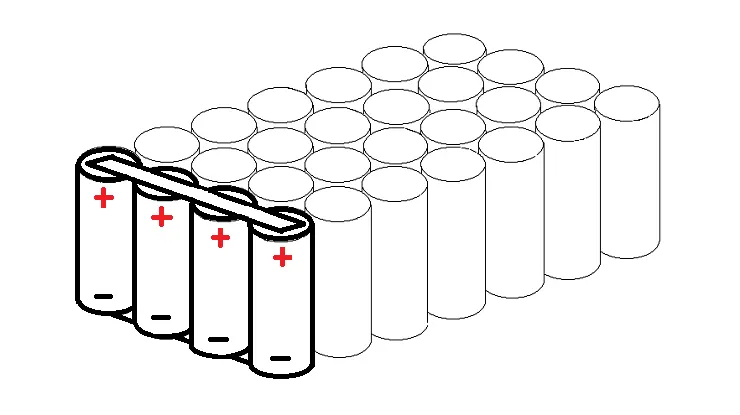
Cells in Parallel connections-
If you take several cells and connect their same-type electrodes in parallel, they all will act as though they are one large cell. Also, when you first connect them to each other,
they must be at the same level of charge.
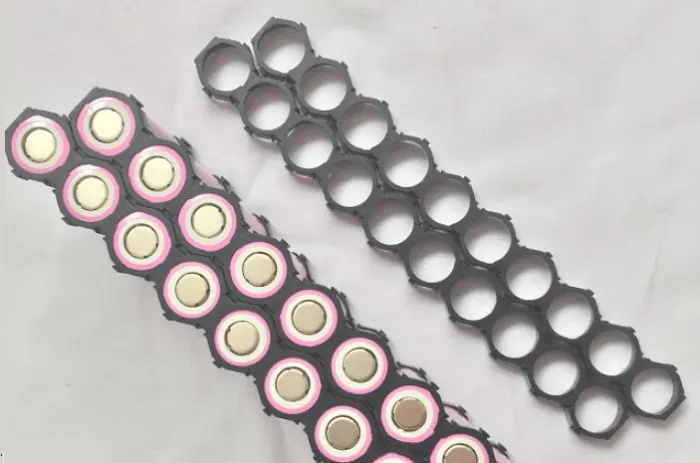
Cell houlders-
These houlders are used for houlding the individual cells in a better posture without mis-assemble.The connections can be made accordingly to make series connections and
parallel connections to form the required module dimensions.
After installind the cells in a individual module the entire maximum positive terminal and maximum negative terninal are made under single pair of
terminals as shown below.
Here shown the cells are arranged and welded without using cell houlders as,
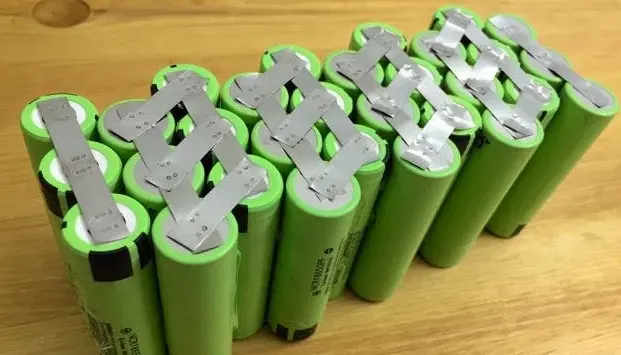
They are just covered by polimer sheet after the interconnections are made. Mostly connections with cell holders should be recommanded for better
safety concerns.
Battery Cabinet arrangements-
Each modules are interconnected in series or parllel according to the requirement and packed as a single large cabinet pack as shown below.
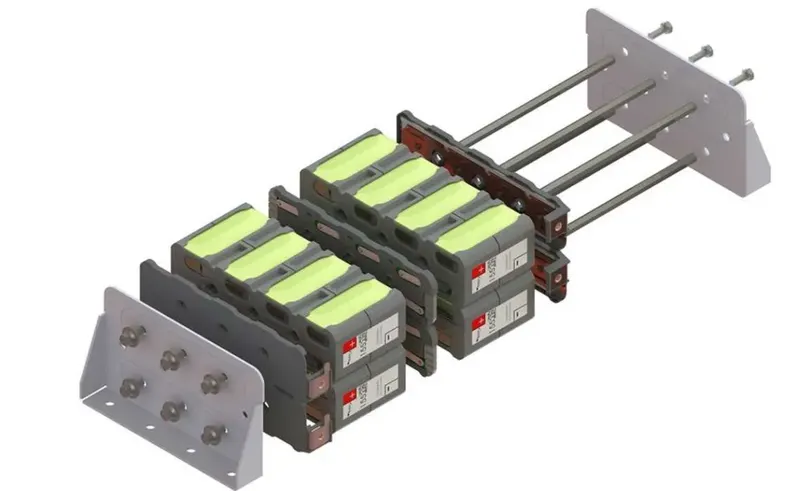
Battery pack arrangement:
Finally the overall battery pack after the arrangement of all cabinet connections with enclosure looks like this as shown below,
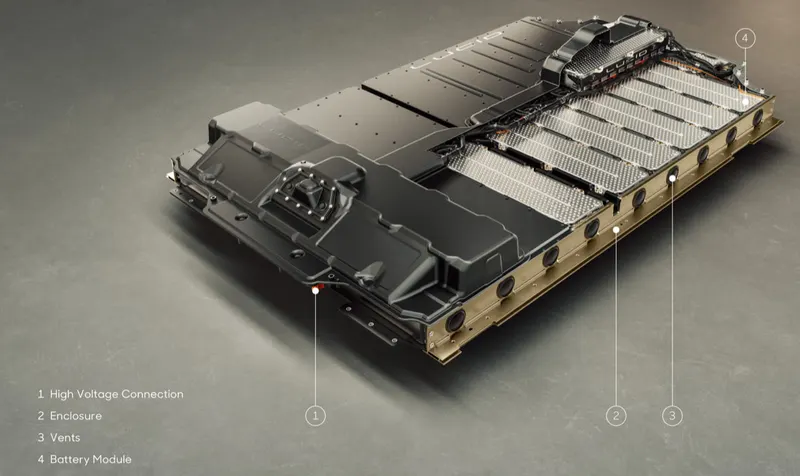
Vents holes are present with enclosure for cooling/heating the battery pack temperature according to its environment conditions.
Different cell types are used by different manufacturers of EV such as Cylindrical,Prismatic,Pouch types.
The pack constructions are different for every manufacturers.
Below shown the battery pack constructios process of Tesla,BMW and Nissan Leaf.
Conclusion:
Lithium Ion and Lithium Ion Polymer batteries are a great power source for some applications but they require preventive protection during discharging and charging.