Design of backdoor
DESIGN OF BACKDOOR
AIM:-
To design the Back door as per the given skin requirements and also provide reinforcements for hinges, Latch, Gas stay, and wiper motor mounting areas.
INTRODUCTION:-
The back door of the car is one of the closure commodities of a vehicle that is present at the back portion of the car. While designing the back door space requirement, a luggage room is also present in this region.
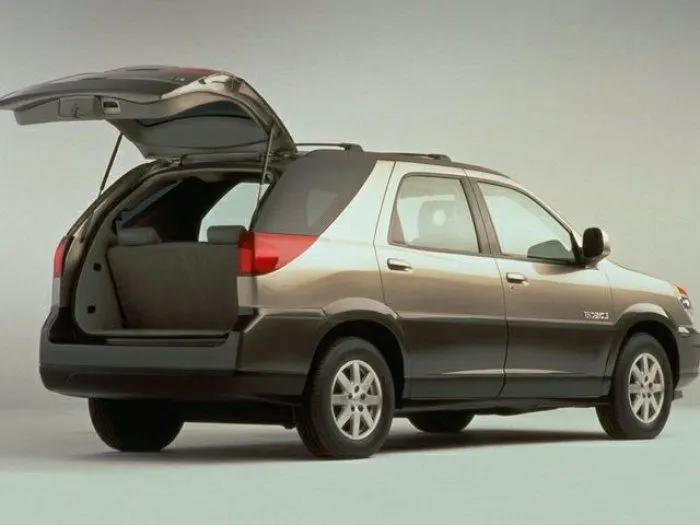
Design Consideration:
- Rear Visibility
- Latch and Striker Reinforcement
- Hinge and Gas Stay Reinforcement
Design Methodologies:
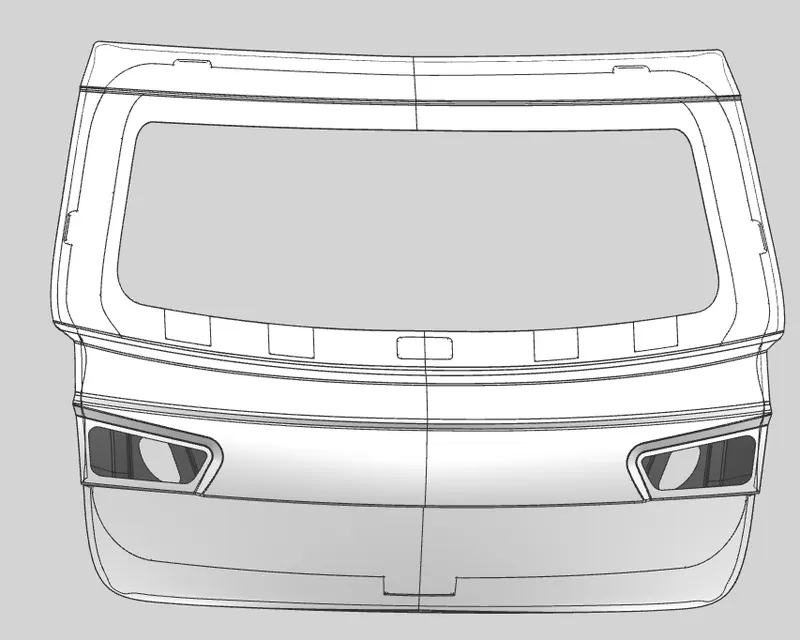
- Outer Panel: The outer pannel is the styling surface of the back door. It is a source of the outer parts of the back door. It gives more aesthetic to the car. Its thicken is in the range of 0.65-0.75 mm.
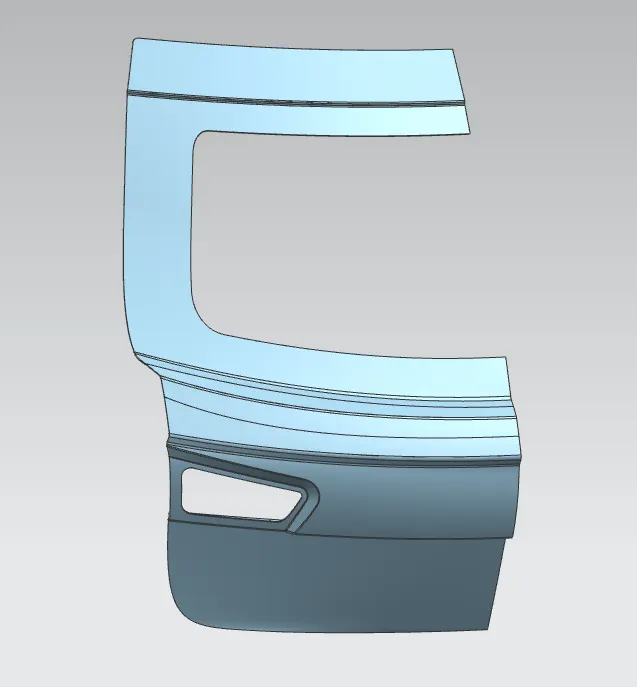
The above surface was analyzed and it was observed that the surface provided was having uneven surface quality.
- Inner Panel: The inner panel provides strength to the back door. There are many cases where the inner panel is subject to stress due to features opening and slamming. These stress factors are compensated by features like embossing and reinforcements. It also has a thickness range from 0.65-0.75 mm.
Determination of Tooling Axis:
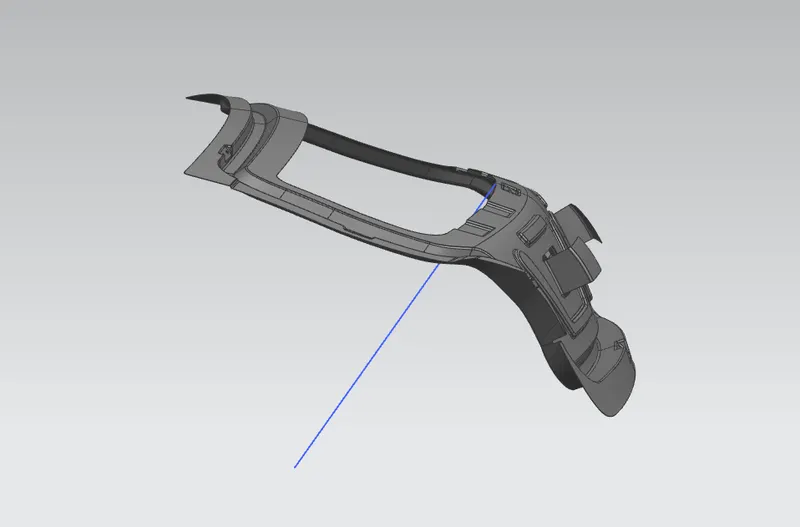
The tooling axis plays an important role while making a component. It is the axis of the line along which the components will be extracted after the component is been molded.
In this project, the tooling axis is made by making two lines touch the opposite ends of the styling surface, and then a bisecting line is drawn between these two lines to determine the tooling direction.
Determination of embossing shape and direction:-
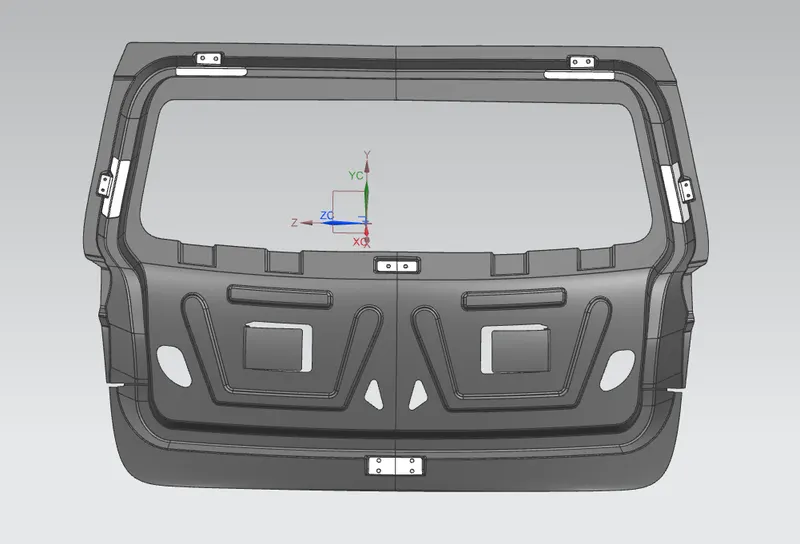
As the back door opens and closes in the upwards and downwards direction, during this time force is generated on it which might affect the durability of the back door panel. This generated force is dissipated in the outwards direction with the help of creating an emboss as shown in the below fig.,
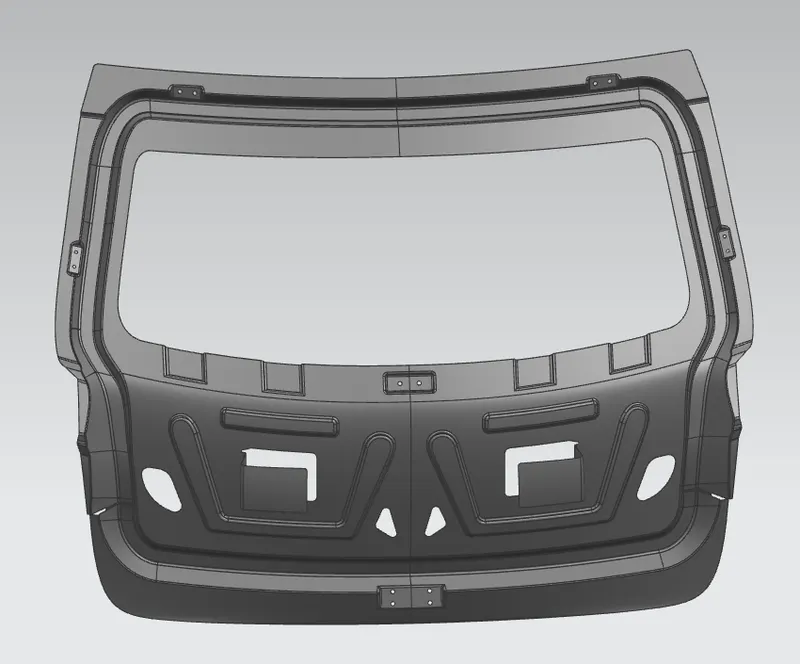
To firmly fix the outer panel to the inner panel a mastic extension flange is protruded towards the outer panel direction so that mastic can be applied on it and then the outer panel and inner panel will behave more strength in the middle portion and be stuck with each other firmly.
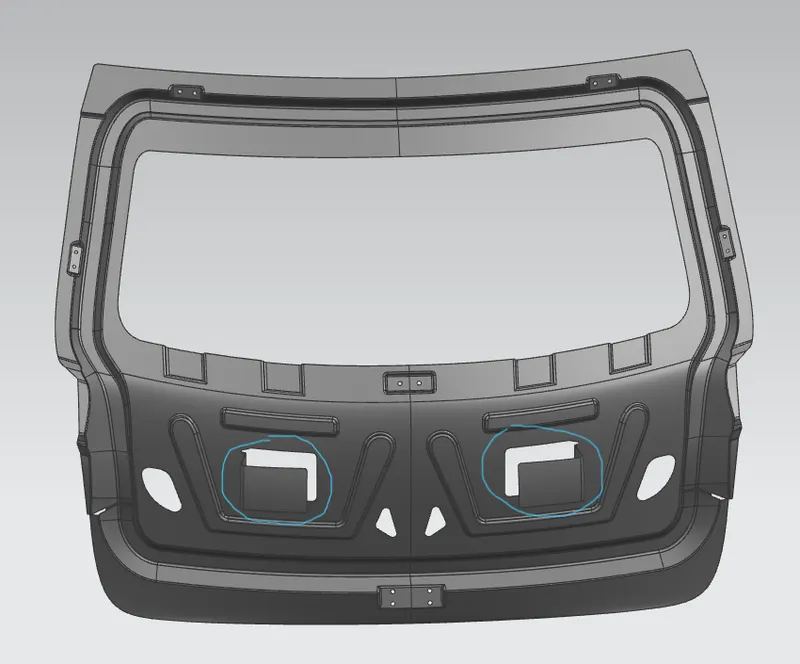
The above image shows the position of the flanges on the back door inner panel.
Embosses:
To provide strength to the inner panel, various embosses are designed on it to fix the reinforcement on the inner panel firmly.
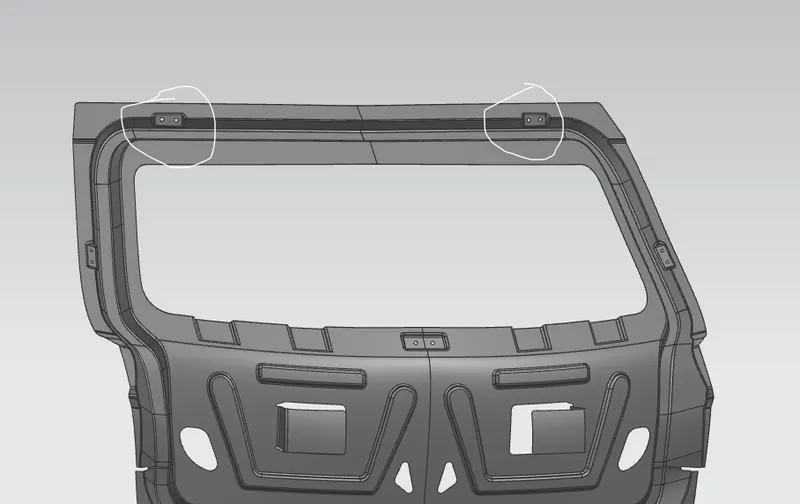
- Hinge Emboss
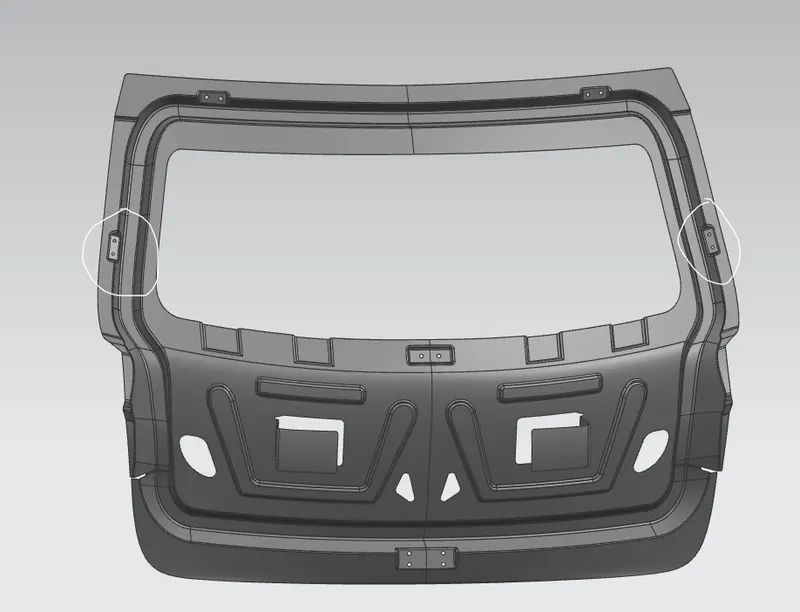
- Gas Stay Emboss
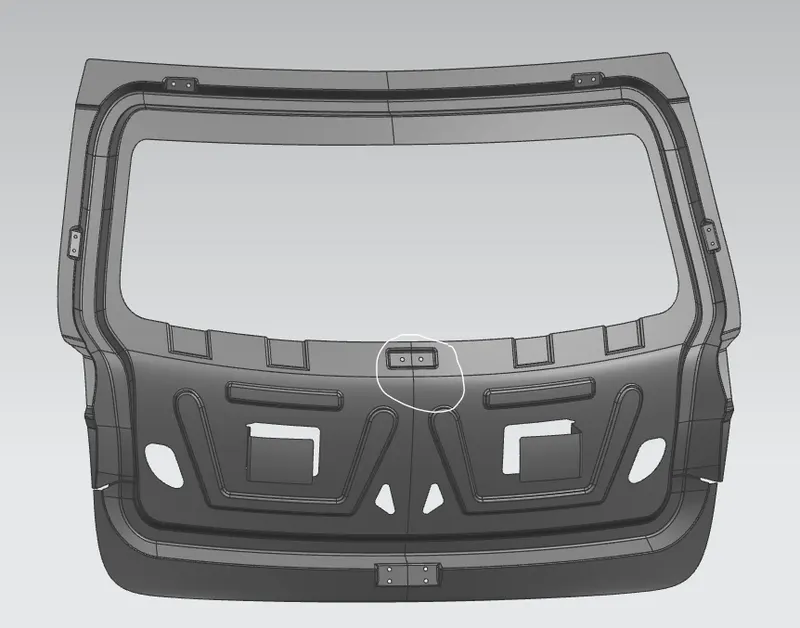
- Wiper Moter Emboss
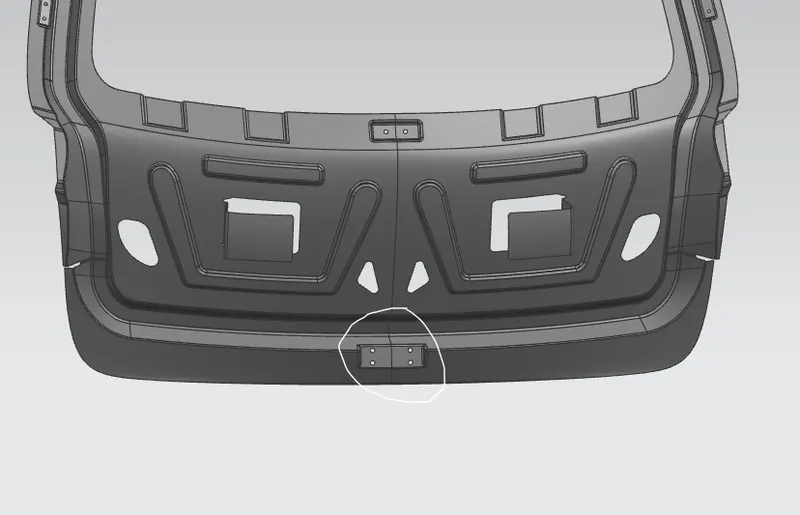
- Latch Emboss
Hinge Emboss: Hinges are placed at the top of the inner panel on the left side and right side to fix the hinge to the inner panel embosses are designed on the back door inner panel.
Gas Stay Emboss:
Gas stay is the component that is used to lift and lower the back door automatically with the help of pressing a button. This is placed on both the left and right sides of the back door.
Wiper Motor Emboss:
The wipe motor emboss is designed at the middle of the back door where the wiper motor will be placed on the back door. To clean the glass of the back door, this mechanism is used on the back door.
Latch Emboss: This embossing is designed at the bottom portion of the back door. This system is used for locking the back door to the car.
REINFORCEMENTS
Reinforcements are the components that are used to add strength to a particular region.
The reinforcement designed for the back door is
- Hinge Reinforcement
- Gas Stay Reinforcement
- Wiper Motor Reinforcement
- Latch Reinforcement
- Hinge Reinforcement: The Hinge Reinforcement will be placed on the emboss of the hinges which will enable it to fix the reinforcement firmly to the back door at the required position.
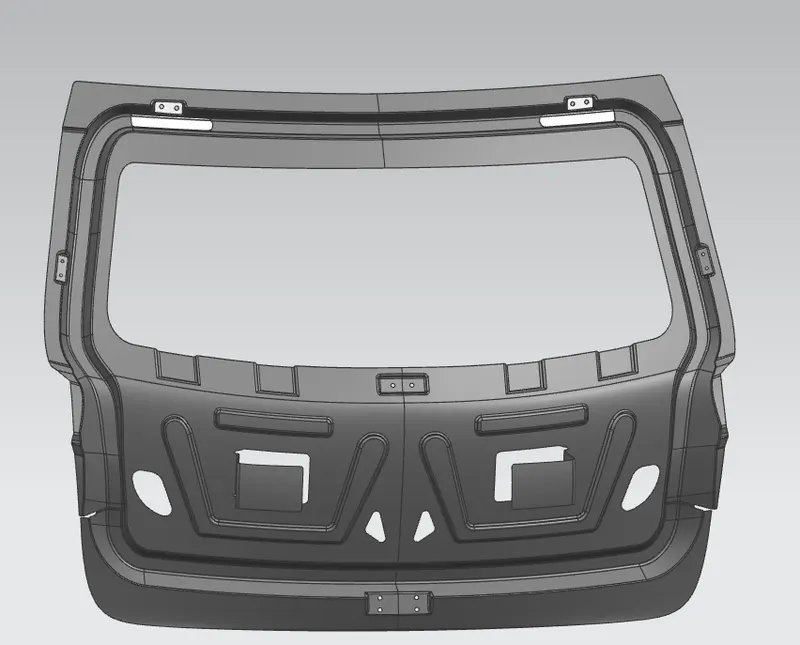
Gas Stay Reinforcement: Gas stay reinforcement is designed to provide strength to the region where the back door will be get opened and closed with the help of a gas stay rod. For durability, these reinforcements are placed where the gas stay will be fixed with the back door panel.
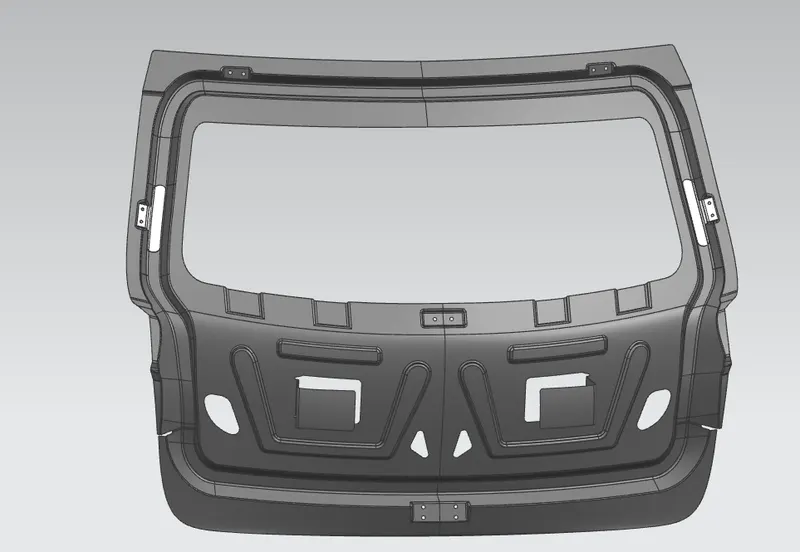
Wiper Motor Reinforcement: Wiper Motor Reinforcement is placed at the middle portion of the back door to provide strength in this region for the placement of the wiper motor.
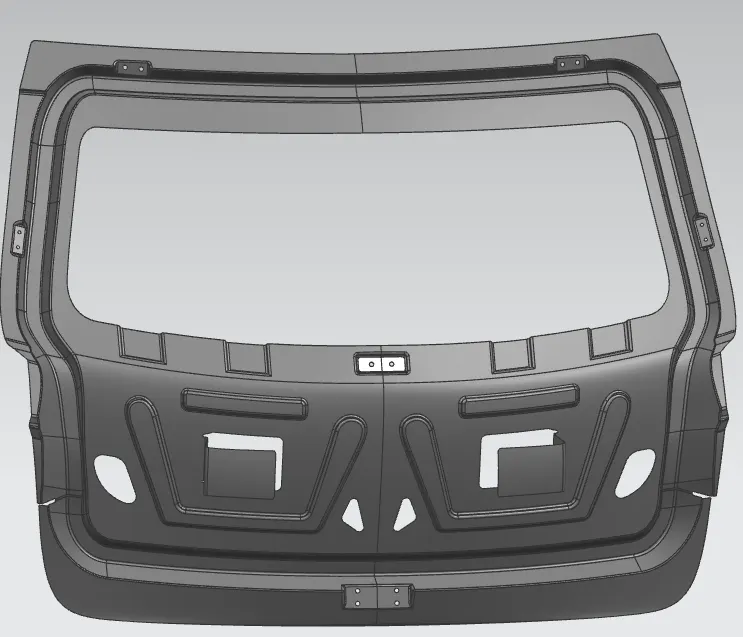
Latch Reinforcement:
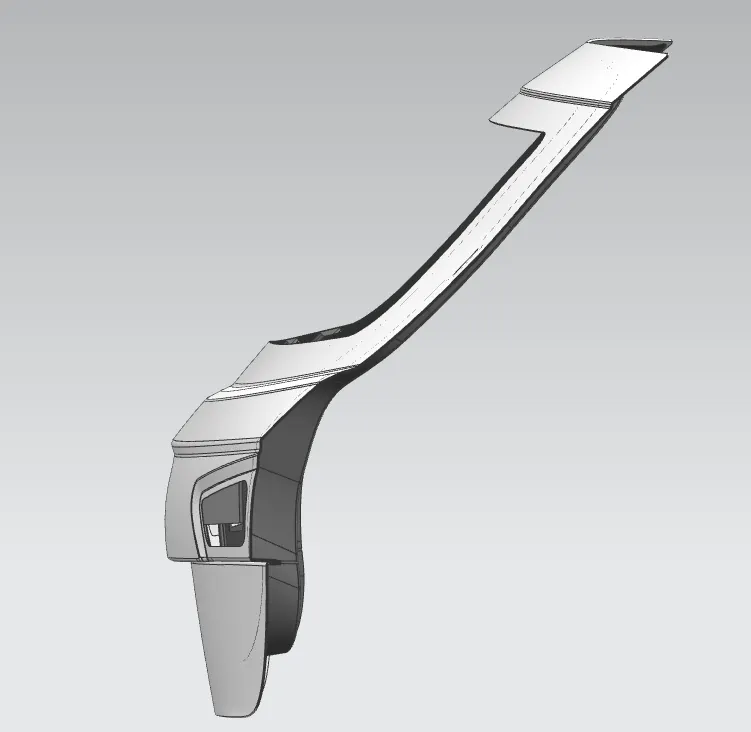
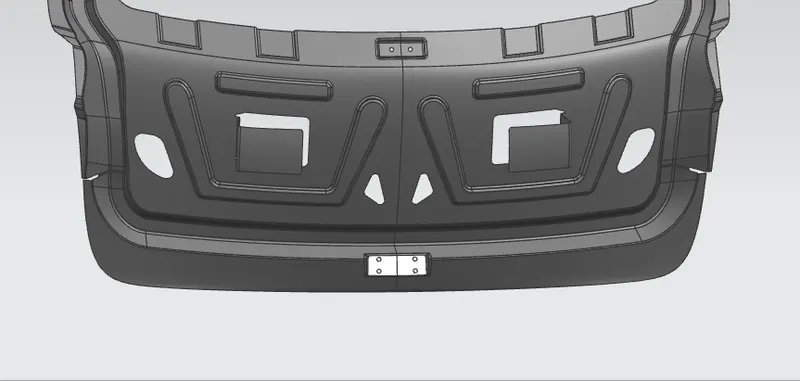
To place the latch at the correct position, the latch position is perpendicular to this circular trajectory at all the positions of the movement of the back door. To provide strength in this region, a latch reinforcement is placed which is shown in the below image.
HEMMING REGION:
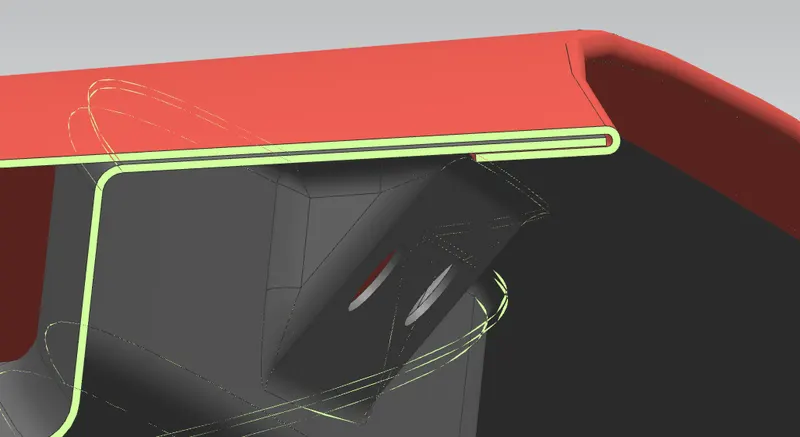
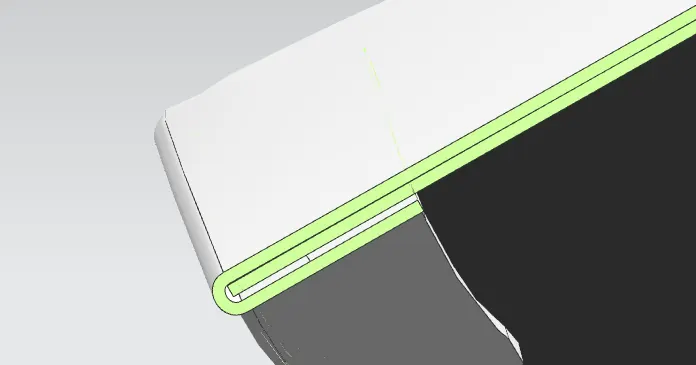
The back door outer panel will be fixed with the back door inner panel with the help of hemming which will be done on the outermost edges of the outer panel. In this process, the surface is bent and rounded around the inside surface so that it firmly holds the inside panel. Along with this music, the solvent will also be inserted into this region for firmly sticking the outer panel with the panel.
CORNER RELIEFS
DRAFT ANALYSIS:
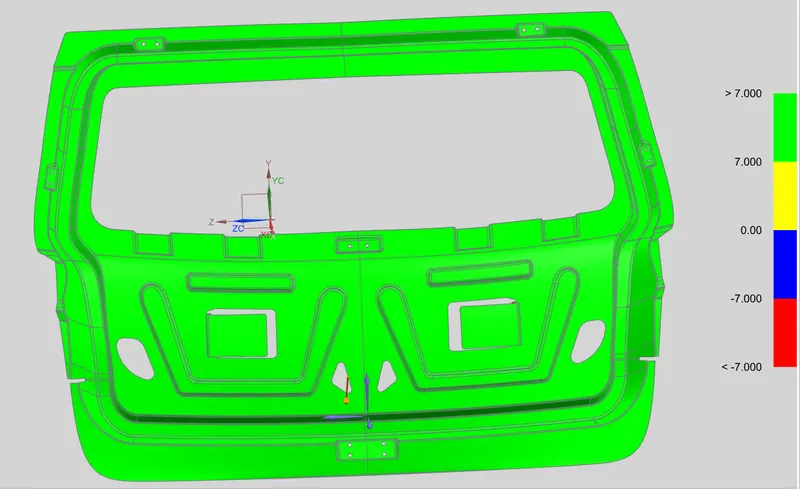
Draft Analysis of the inner panel is carried out through the tooling direction only. Only the green areas are acceptable and in some other worst cases yellow regions are acceptable but the blue and red regions are never accepted.
The drat angle for the aluminum casted panel is 2 to 3 degrees is enough but if it is steel then the angle is more than 7degrees.
In this project, I considered it as steel and used 7 degrees as draft angle and direction I was chosen as tooling direction which is the deep-drawn direction.
Joining Techniques:
Deep Drawing:-
Deep drawing is one of the most widely used processes in sheet metal forming. Apart from its use in many other sectors, it is applied in the automotive industry for the manufacturing of car body parts.
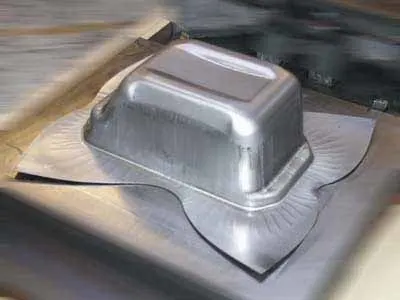
- It consists of die, punch, blank holders.
- After the application of drawing force, the blank of material forms & takes shape of the punch or shape made onto the punch. To avoid frictional resistance between blank & die, lubricant is used.
- The applications of the deep drawing process are kitchen utensils, cylindrical containers, fire extinguishers
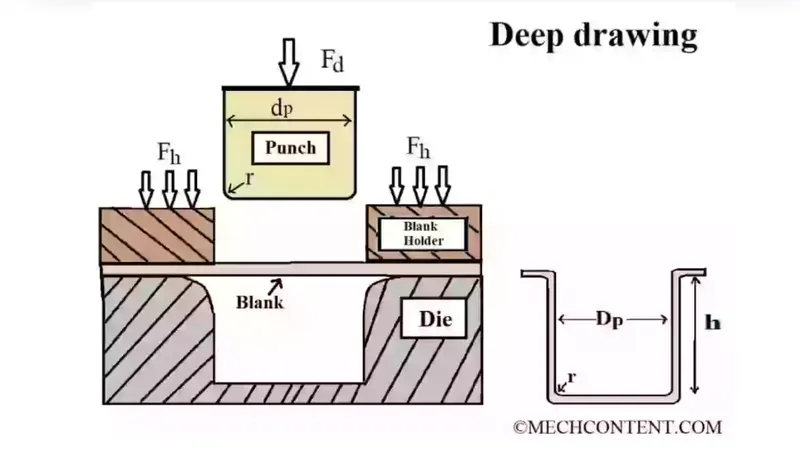
The Deep Drawing is shown above image.
Hemming:- Hemming is a forming operation in which the edges of the sheet are folded or folded over another part to achieve a tight fit. Normally hemming operations are used to connect parts, to improve the appearance of the part, and to reinforce parts edges.
In-car parts production, hemming is used in assembly as a secondary operation after deep drawing, trimming, and flanging operations to join two sheet metal parts (outer and inner) together Typical parts for this type of assembly are hoods, doors, trunk lids, and fenders.
There are various types of hemming operations:
- Conventional die hemming
- Roll hemming
Conventional die hemming:-
In conventional die hemming, the flange is folded over the entire length with a hemming tool. production plants for conventional die hemming are very expensive, but the cycle times are very low.
Roll Hemming:-
In roll hemming, the hemming roller is guided by an industrial robot to form the flange. Roll hemming is very flexible to use and tool cost are significantly lower as compared to die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller that follows a defined path.
SPOT WELDING:
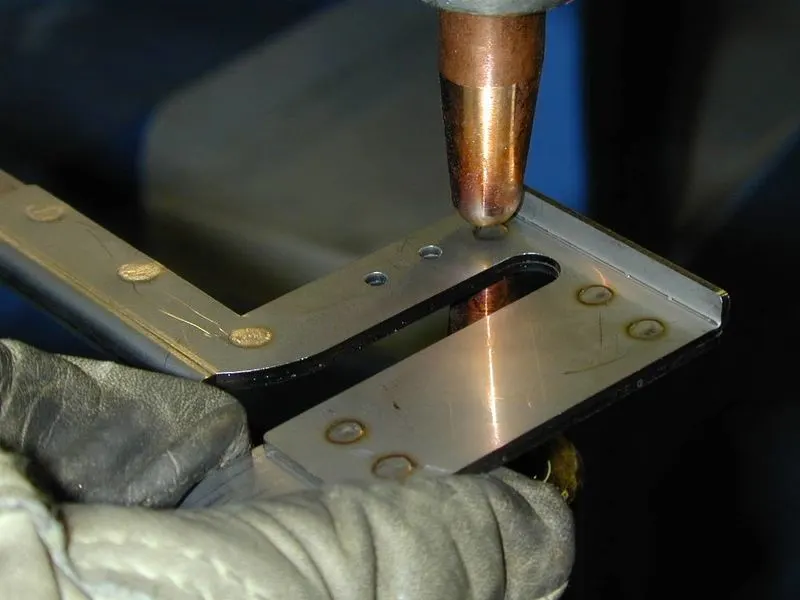
Spot welding is a form of resistance welding also known as Resistance Spot Welding(RSW). Spot Welding involves using heat produced by resistance to an electrical current to join materials together. The current heats the material to a point where they become malleable. The use of strong pressure bonds them together.
Another form of resistance welding is projection welding. The process involves fusing fasteners embossed or coined projections to the metal base material to form a weld. The outer panel upper and outer panel lower are joined through the spot welding. So there must be no gap between the outer panel upper and outer panel lower.
LASER BRAZING
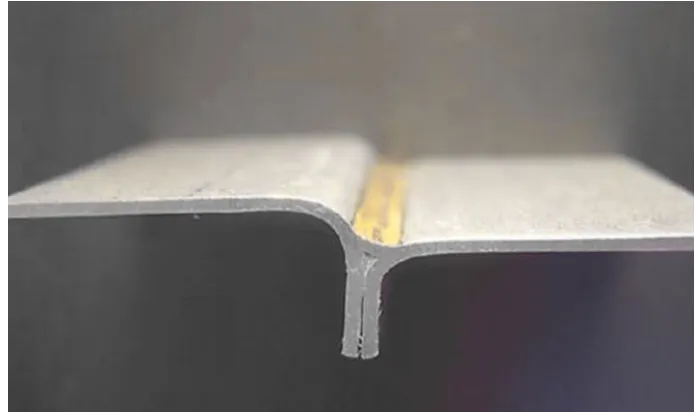
Laser brazing is a joining process for sheet metals where the filler material with a low melting point is melted with a laser beam while the base material with a higher melting point does not melt. In laser brazing, the working temperature is above 450 c while another process is laser soldering, where the working temperature is below 450 c. Laser soldering is used especially in the electronics industry in soldering circuit boards.
CONCLUSION:
So as per the objective, the back door is designed for the given panel.