Design of backdoor
BACK DOOR DESIGN
AIM:
- To design the back door of the car and make the inner panel for the back door and also design the necessary reinforcements.
SOFTWARE: NX
INTRODUCTION:
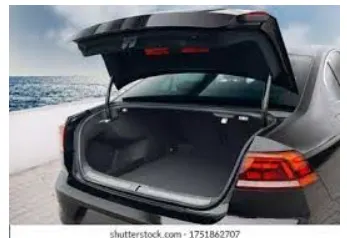
- The Trunk (North American English) or Boot (British English) of a car is the vehicle's main storage or cargo compartment, often a hatch at the rear of the vehicle. It is also called a Tailgate. These doors can be operated manually or electric powered. In most of the luxury cars door is electrically operated. It involves a very major role during rear crash cases. So our design must obey crash requirements. The institute of highway safety analyze the different accidents and they set a test to rate the car. So these rating depends upon the design of the trunck and material used, flanges, embosses, type of joining of inner panel and outer panel etc.
fig(1)
- Types of door based on working position:
- Top Mounted Door
- Side Mounted Door
- Bottom Door
fig(2)
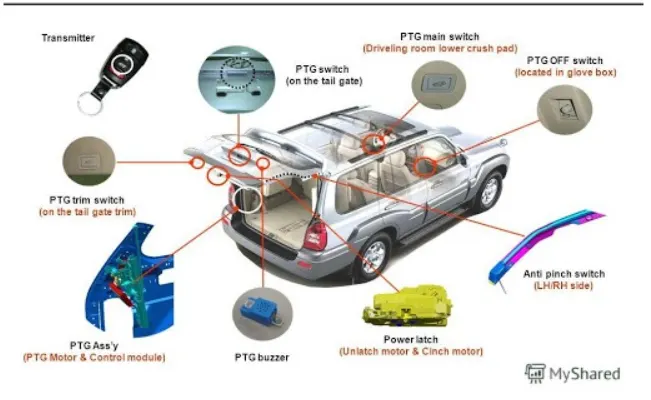
The Back Door is operated by two types of comodities:
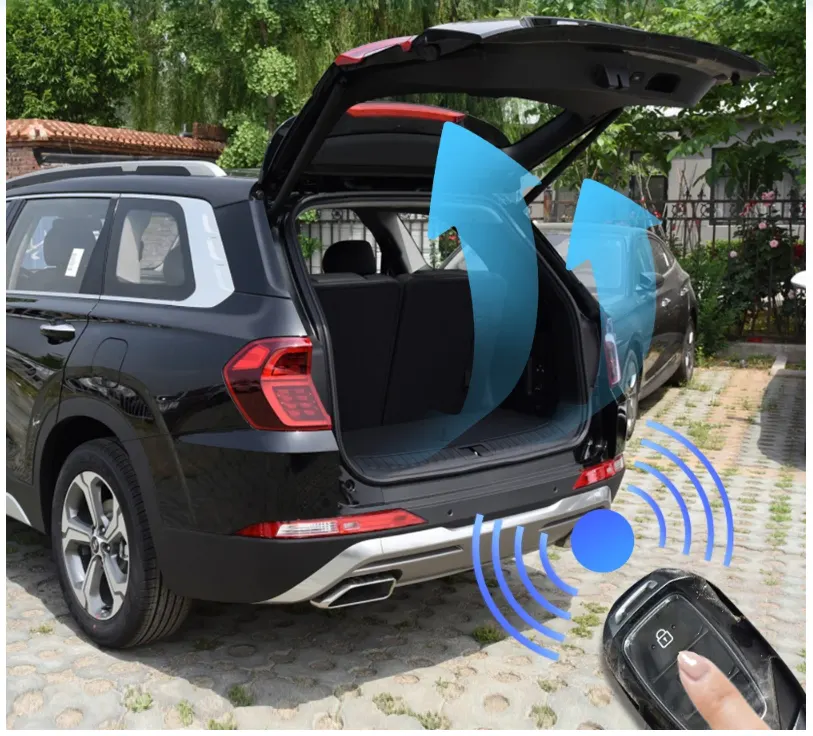
- Electrically operated
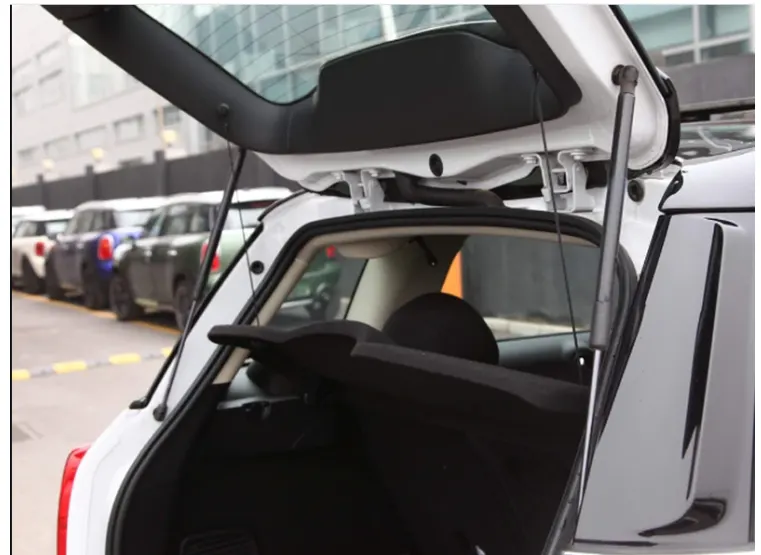
- Gas stay powered
- The main purpose of these mechanism is to open the back door without heavy efforts, because the backdoor have different parts and the weight of the back door is high, so we are not able to open the back door manually, so we introduced these two types comodities. These comodities also decides the premium of the car, mostly the electrically operated used in premium cars.
GAS STAY POWERED:
fig(3)
ELECTRICALLY OPERATED:
fig(4)
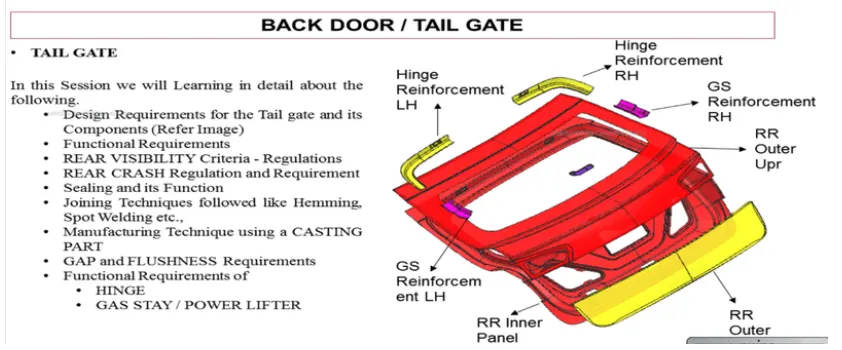
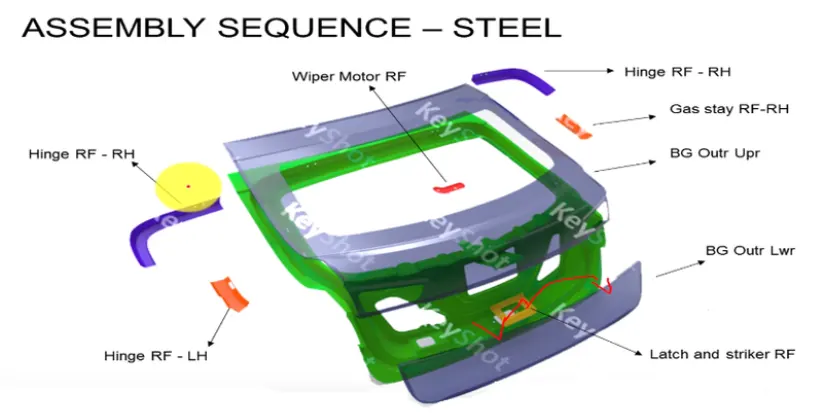
BACK DOOR ASSEMBLY:
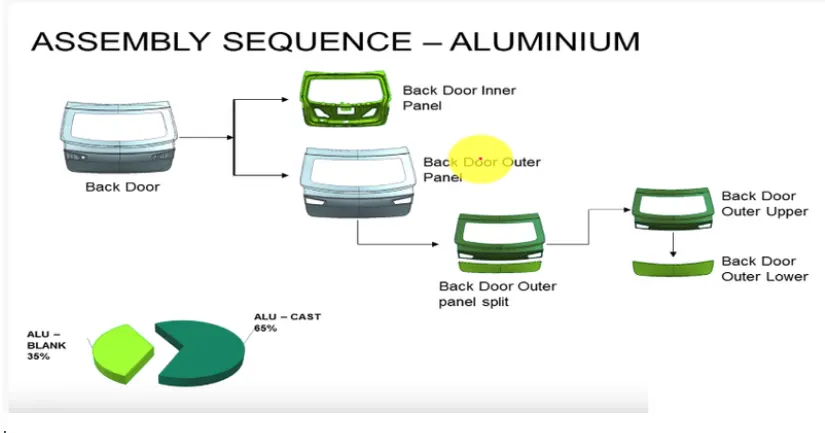
- Inner Panel
- Outer panel
- Hinge and its reinforcements
- Wiper motor reinforcements
- Latch & Striker and its reinforcements
- Gas Stay reinforcement
fig(5)
- The major problem in back door is material selection. Mostly in past days Steel is used, but it comes with some drawbacks that it is heavy in weight, due this reason the fuel efficiency is less. Insted of steel presently in high end cars aluminum is used, the major objective of aluminum it have less denser material and suitable for complex shape, it also gives thickness locally because it is done casting in case of steel we use deep drawing operation. There are some advantages and disadvantages are there:
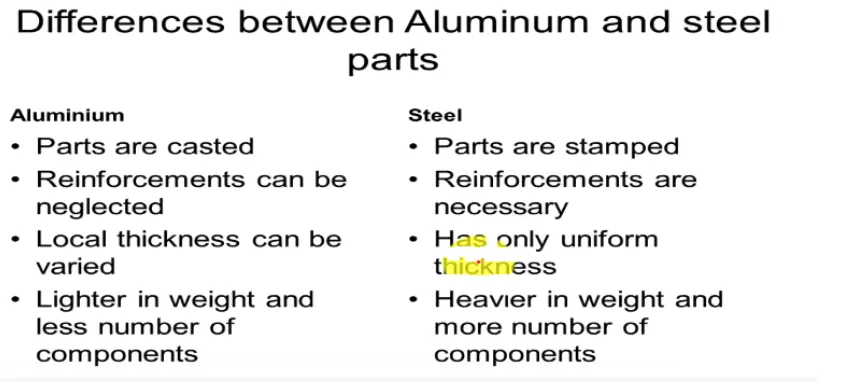
- So by using aluminium we can reduce the number of parts and assembly involvement and it is castly material.
fig(6)
fig(7)
Different types of Sheetmetal operation in Back door:
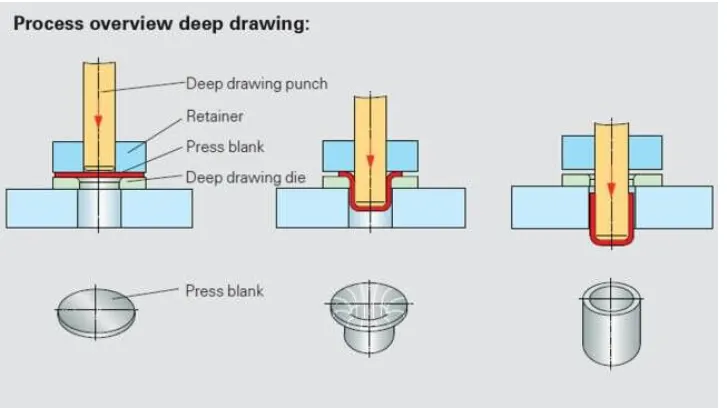
DEEP DRAWING:
- The metal deep drawing process is an effective method of manufacturing of cup,cans and other similar deep drawing products. The deep drawing having two main categories.
FIRST-STAGE DRAWING:
- The blank shape of metal is placed on the die and contact it with the punch.When the metal specimen is flat piece of sheet metal used in forming and finish the product .Initially the punch moves in downward direction. The outter rim of blank is subjective to pure radial drawing (Drawing toward in vertical axes) Between die an blank metal. The metal become bend and slide over die and also streched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and strech over punch head.
REDRAWING:
- The components drawn from first stage, redrawn again to covert into more depth to get a cup shape in the die and punch.The second stage of drawing is known as Redrawing.
fig(8)
EMBOSSING:
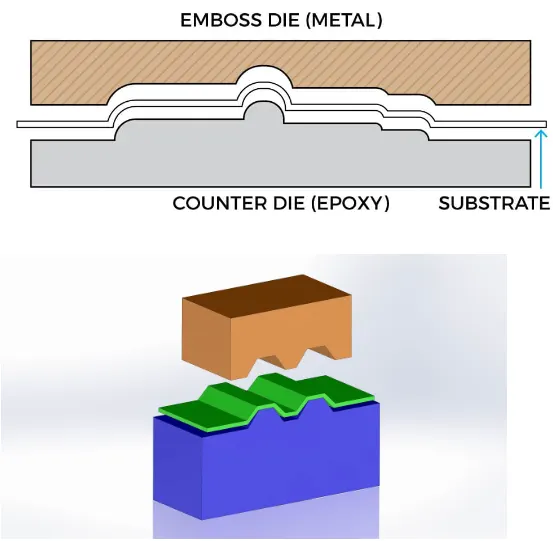
- Embossing is a metal forming process for producing raised or sunken design or relief in sheet metarials by means of matched male and female rollers dies,theoretically with no change in metal thickness or by-passing sheet or strip of metal between rolls of the desired pattern.Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used , different patterns can be produced on the metal sheet.
- Material commonly used in the metal Embossing process include:
- Aluminum alloys
- Steel alloys
- Zinic
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
fig(9)
HEMMING:
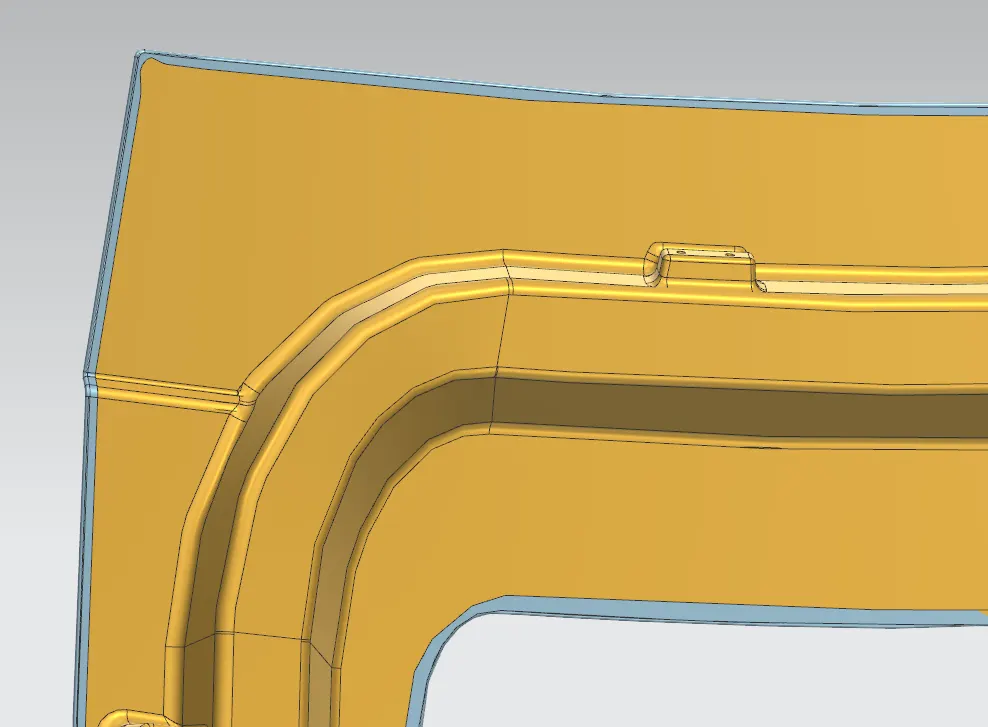
- Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
- In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming, flanging operations to join two sheet metal parts(outer and inner) together. Typical parts for this type of assembly are door, hoods, trunk lids and fenders.
There different types of Hemming operations:
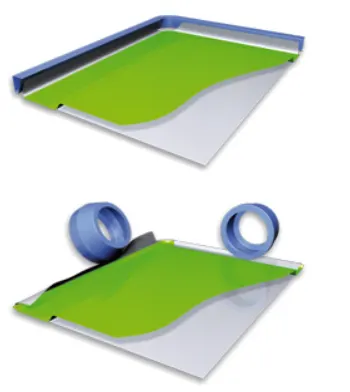
1. Conventional Die Hemming:
- In this the flange is folded over entire length with the help of hemming tool.
2. Roll Hemming:
- In this, the hemming roller is guided by an industrial robot to form the flange.
fig(10)
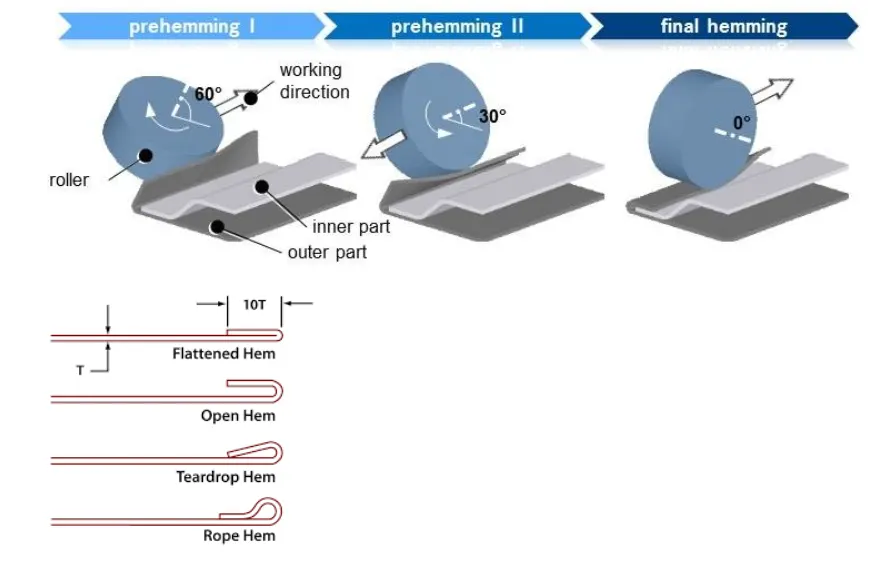
Open Hemming:
- A hemming has a full round feature and a return flange. In open hem bend angle is equal to 180-degree.
Tear Drop hemming:
- In this the bend angle is more than 180 degrees.
Closed Hemming:
- Hem without any inside radius are called closed hemming. Closed hem are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
fig(11)
BLANKING:
- It is a cutting operation of a flat metal sheet and the article punched out is known as Blank. It is the required product of the operation and the metal left behind is considered as waste.
PUNCHING:
- It is similar to blanking only the main difference is that, the hole is rquired product and the material punched out from the hole is considered as waste.
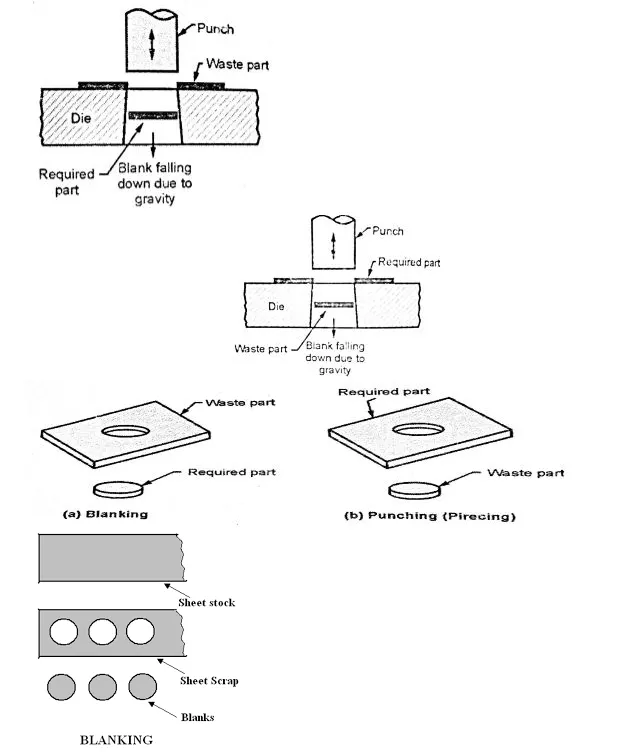
fig(12)
- Inputs for Designing Back Door:
- Outer Panel - 0.75mm
- Inner Panel- 0.75mm
- Reinforcement- 1.5mm
CLASS-A SURFACE:
- Back Door outer upper and lower class surface has to be repaired according to the smoothness. After repairing the surfaces, the door is divided into two parts as the Door outer upper and Door lower panel.
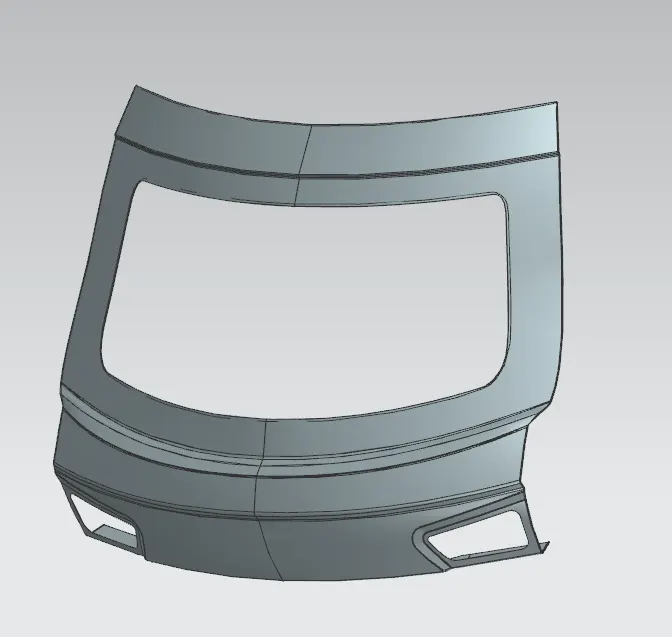
fig(13)
- First, we need to create the Tooling axis for the deep drawing operation. It shows that all operation like Embossing is done by considering the vector direction it will help in manufacturing the part.
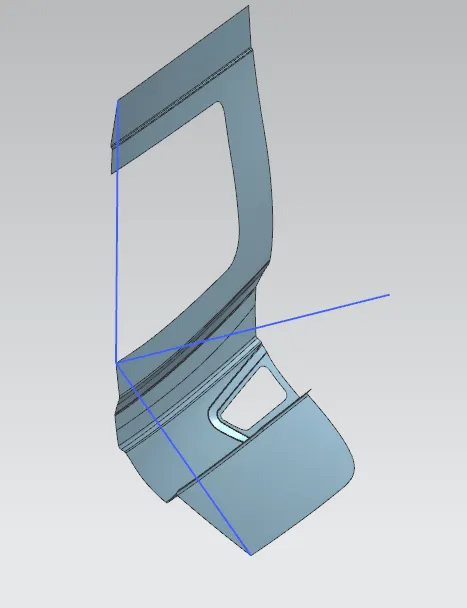
fig(14)
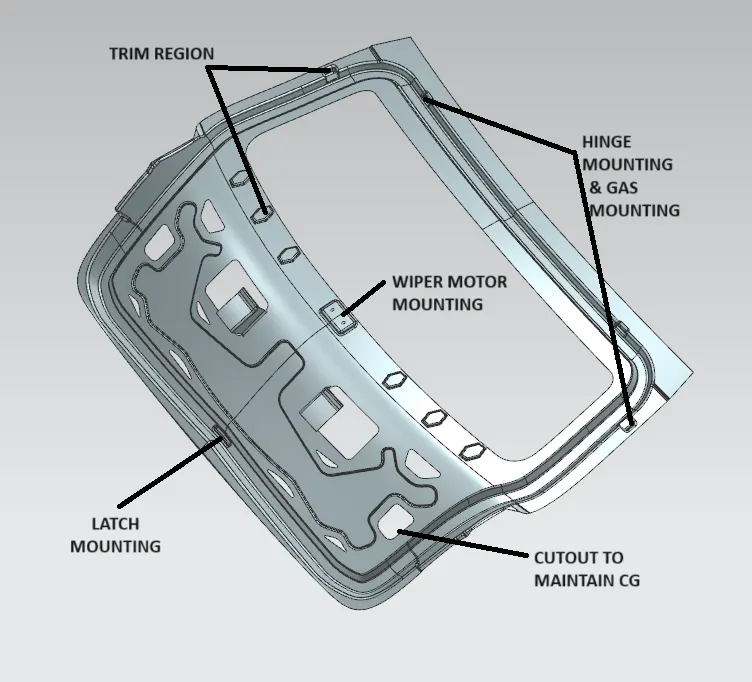
- After that we have to create sealing flange by offseting the outer to the specific distance.
- Then we will be creating the Back door inner panel flange by offseting the outer surface at a distance considering the sheet thickness and thickning direction.
- Then created the connecting flange to join the inner panel and the sealing flange.
- Then for the windshield panel mounting, windshield panel is created and join with the sealing flange.
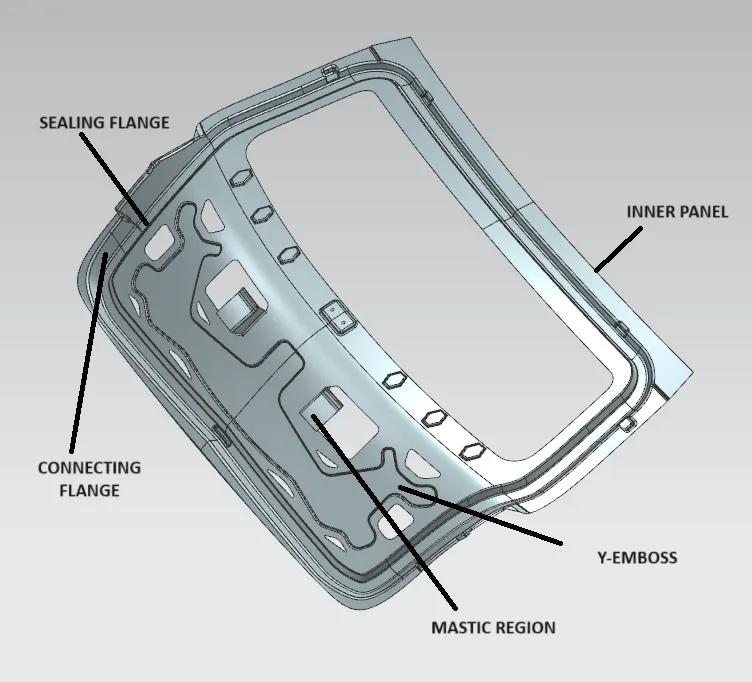
fig(15)
fig(16)
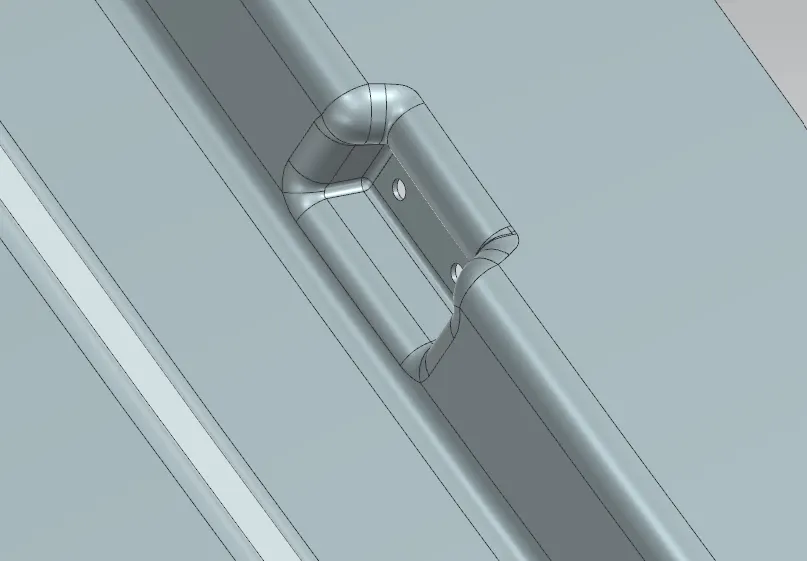
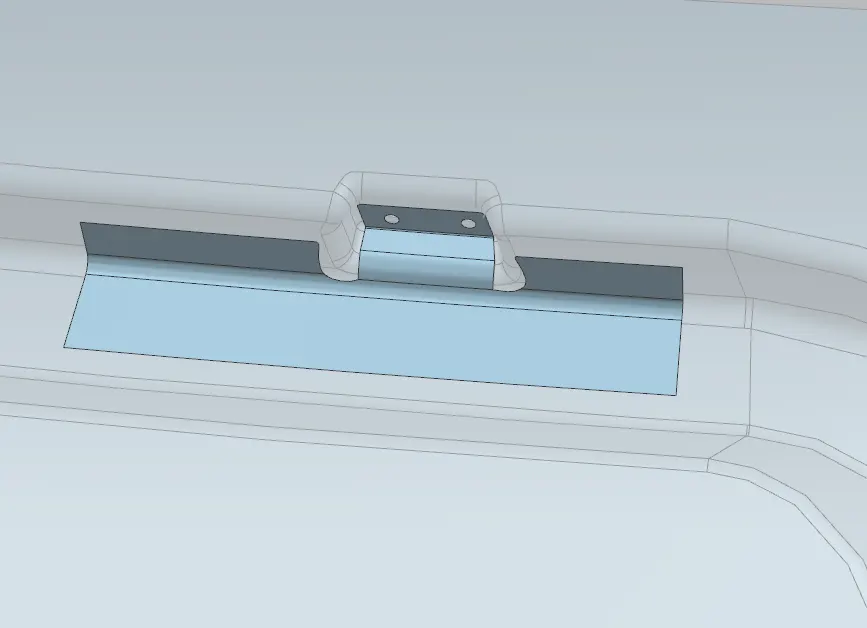
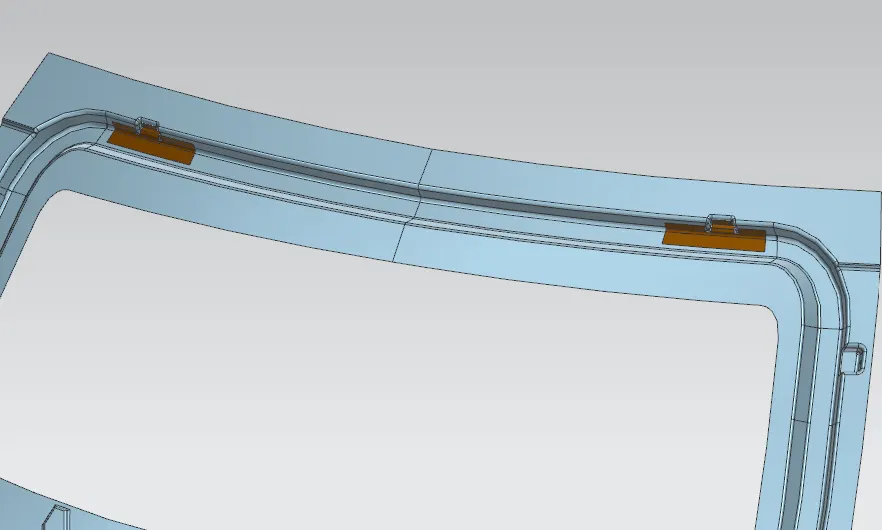
- Now to assemble the Back Door with the vehicle hinges are used to open and close the door. For that to increase the local area strength we have to design the emboss and provide appropriate reinforcement to withstand the load acting upon it.
fig(17)
HINGE REINFORCEMENT:
fig(18)
fig(19)
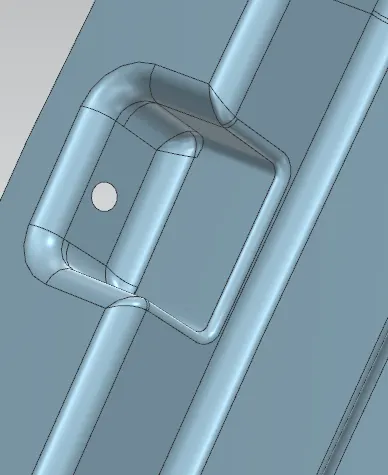
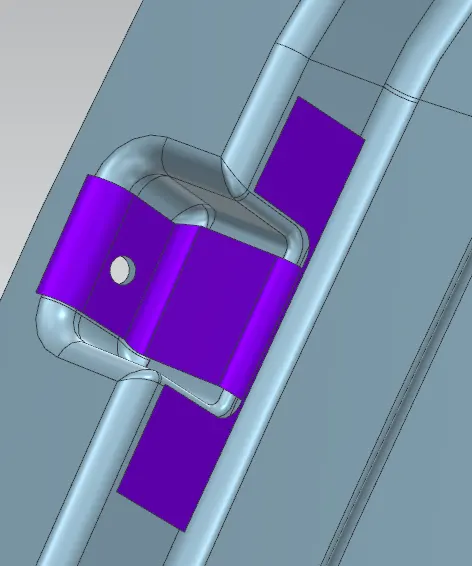
GAS STAY REINFORCEMENT:
fig(20)
fig(21)
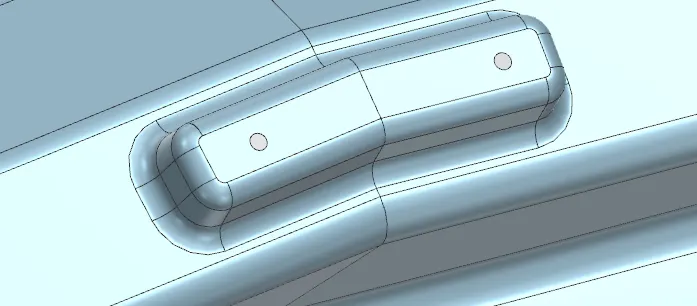
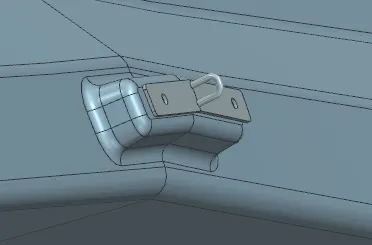
LATCH & STRIKER REINFORCEMENT:
fig(22)
fig(23)
fig(24)
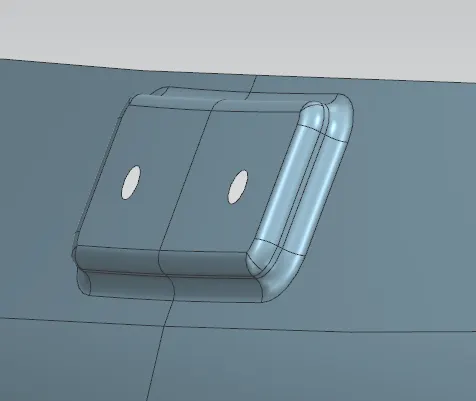
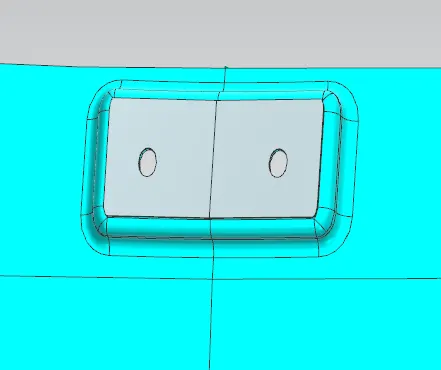
WIPER MOTOR REINFORCEMENT:
fig(25)
fig(26)
HEMMING:
fig(27)
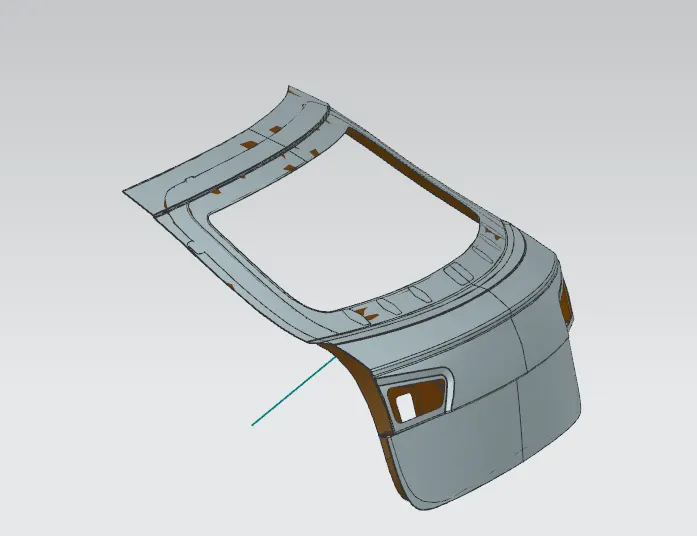
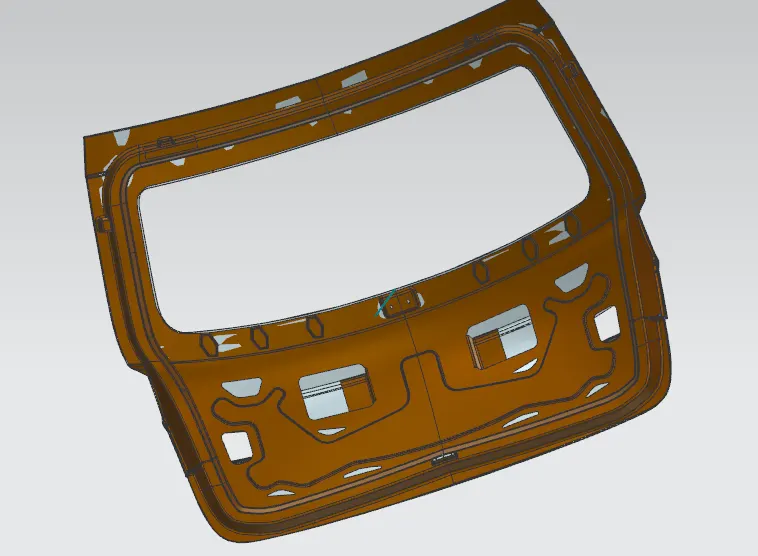
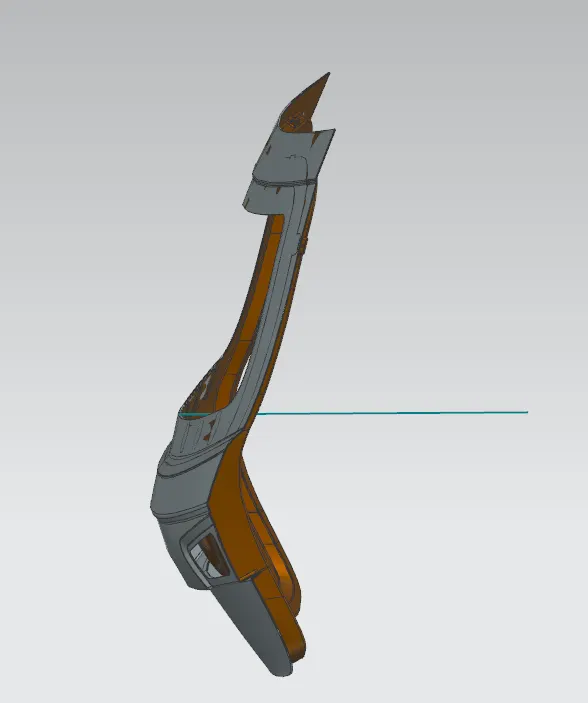
ASSEMBLY:
fig(28)
fig(29)
fig(30)
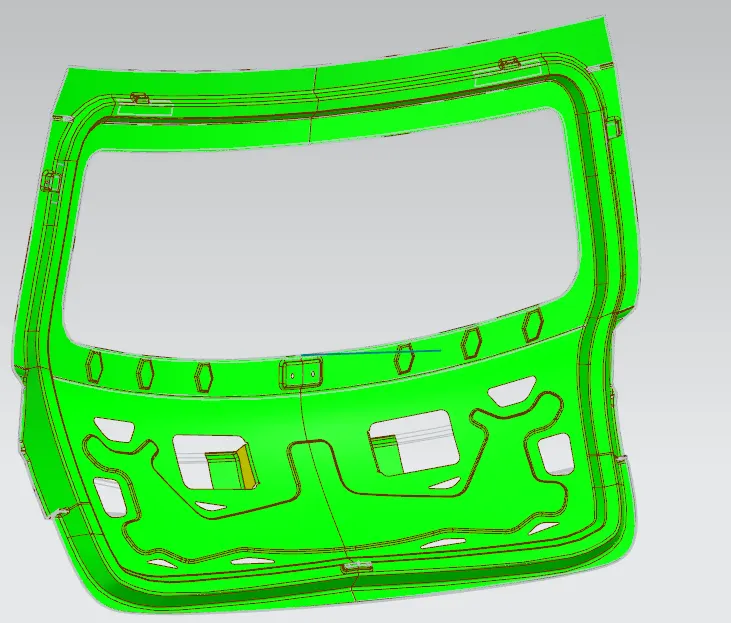
DRAFT ANALYSIS:
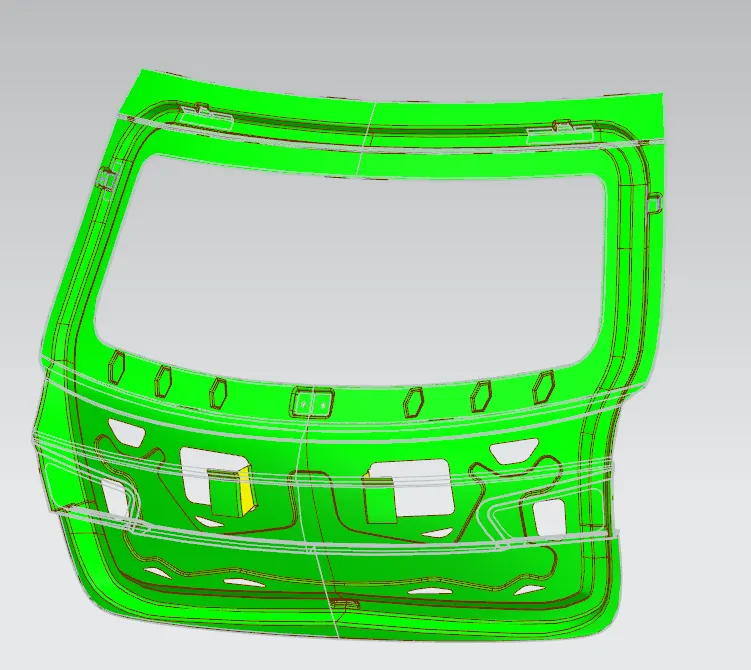
fig(31)
fig(32)
CONCLUSION:
- The Back Door Outer and Inner Panel were designed with the help styling surface along the Toolin Direction. Draft Analysis was performed on inner panel and all the Reinforcements were designed and placed at appropriate positions.
NOTE:- File size is more than 20MB, so the part file link below:
https://drive.google.com/file/d/1Uo52Pit7Z0AU68afmLgJ-SUqkr171sjS/view?usp=drive_link