Design of backdoor
CAR BACK DOOR DESIGN
Aim:
To design a BIW of the Back Door from the given Class A Surfacing. The inner Panel is designed and assembled with Hinge Reinforcements, Gas Stay Reinforcements, Wiper Motor Reinforcements, and Latch Reinforcements.
Introduction:
- In this project, I have designed a back door for a hatchback car where it is hinged at roof level. Similar to the hood and side doors, the back door is a swinging/closure commodity in a car. It consists of an outer and inner panel. It is a very critical component because of the passenger safety requirements.
- The Backdoor has to be designed by keeping in mind the space required for the luggage compartment as well as to accommodate the Latch and Striker motor and Wiper motor without compromising the strength of the component.
- Usually, Aluminium or Steel is used to manufacture the backdoor. While Aluminium backdoor is lighter in weight and has a lesser number of components (since the part is "cast", it has a varying thickness and therefore doesn't require reinforcements). Steel backdoor is "deep drawn" with uniform thickness, and added reinforcements and therefore is heavier. But the production cost of the latter is lesser and therefore a Steel backdoor is priced lower.
Designing and Reinforcement:
Outer Panel:
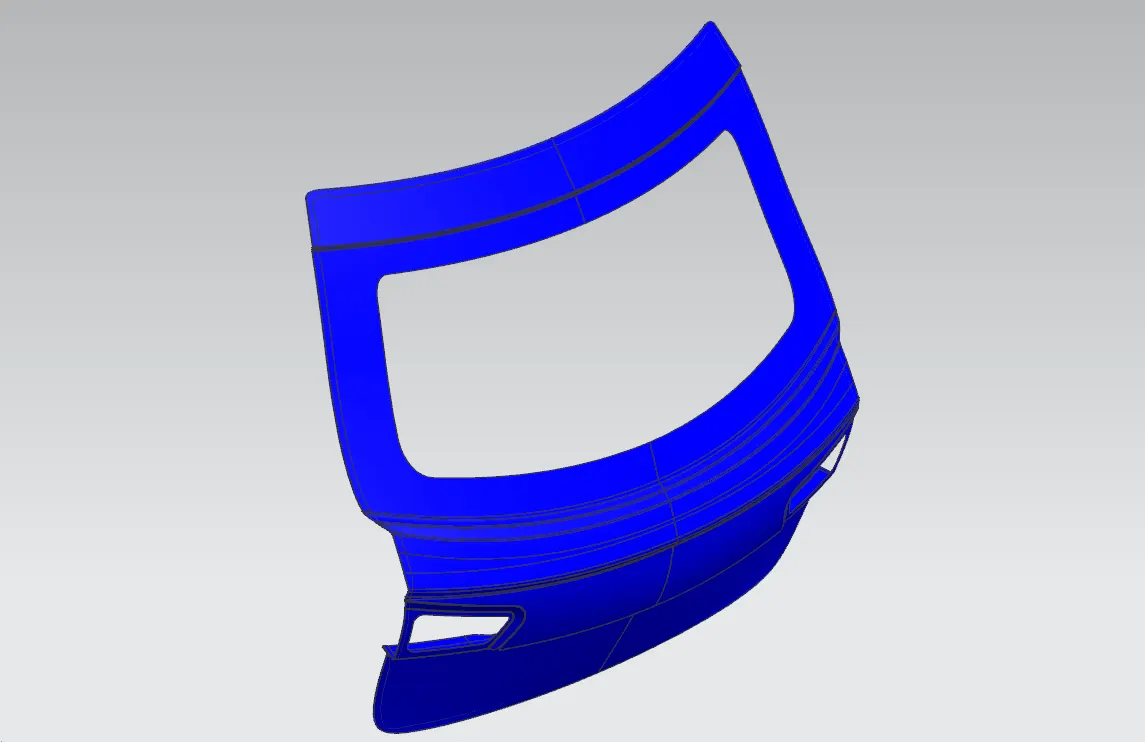
- The Outer Panel is the styling surface of the back door. It is the source of the design of other parts of the back door, primarily the Inner Panel. The Outer panel of the back door is similar to other BIW components where it is the aesthetic part of a vehicle. The coating provided is multi-stage which has the properties of scratch resistance, rush prevention, and smooth and attractive finishes. The Outer panel also has the provisions for the tail lamp, and rear fog lamp and also has the provision for license plate mountings. Most of the hatchback cars have the provision for wiper motors. Its thickness is in the range of 0.65-0.75 millimeters.
Inner Panel:
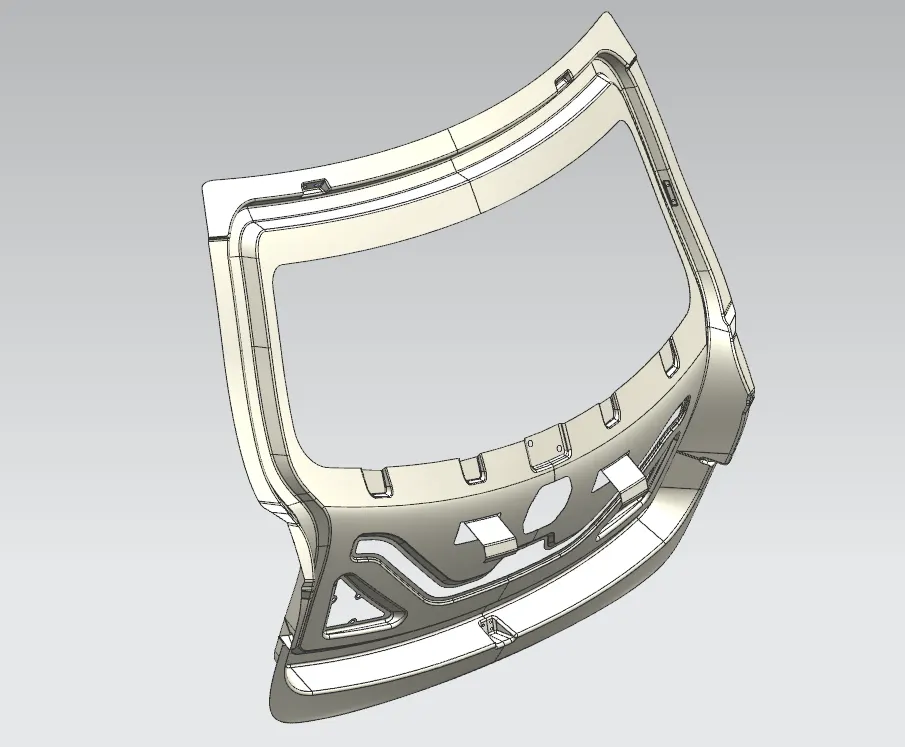
- The inner Panel is a component that is used for strengthening the door. Its thickness is in the range of 0.65-0.75 millimeters. It is one of the most important components on which all accessories are mounted like Hinges, Gas Stay, Wiper Moter, Latch Striker etc.
- The possible method is the integration method. In the integration method, the part is stamped out of a single blank. This reduces the number of tools needed and the assembly cost and eliminates any fit ability problem.
- There are many cases where the Inner panel is subjected to stress due to frequent opening and slamming. These stress and depression factors are compensated by features like embosses and reinforcements.
Reinforcements:
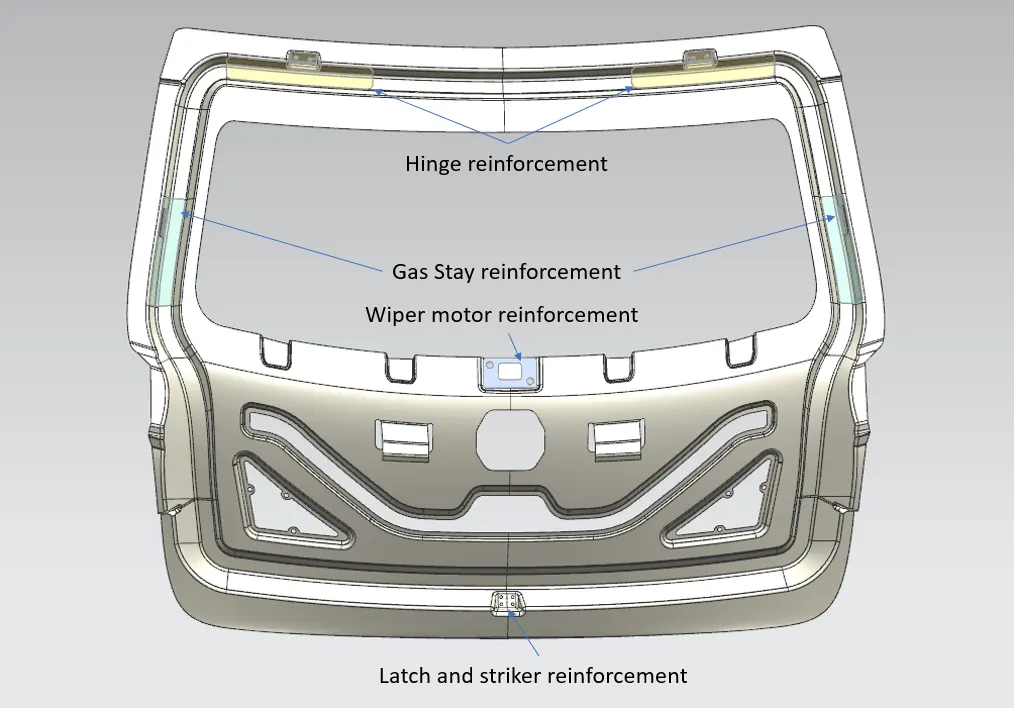
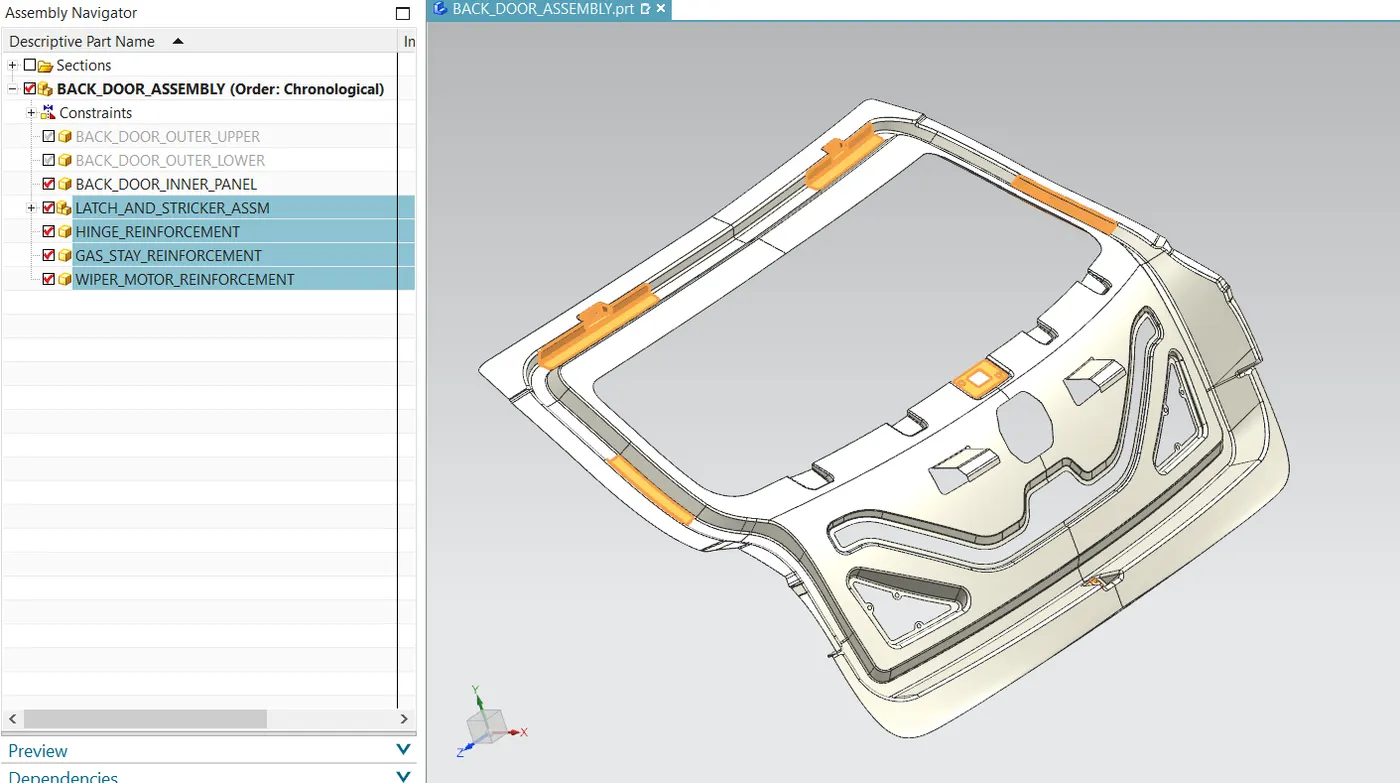
- The inner panel accommodates the Latch and Striker, Wiper Motor, Trims Mounting, Hinge, Gas Stay, etc and therefore the necessary cutouts are provided. Various reinforcements are also spot-welded to the inner panel.
Hinge Reinforcement:
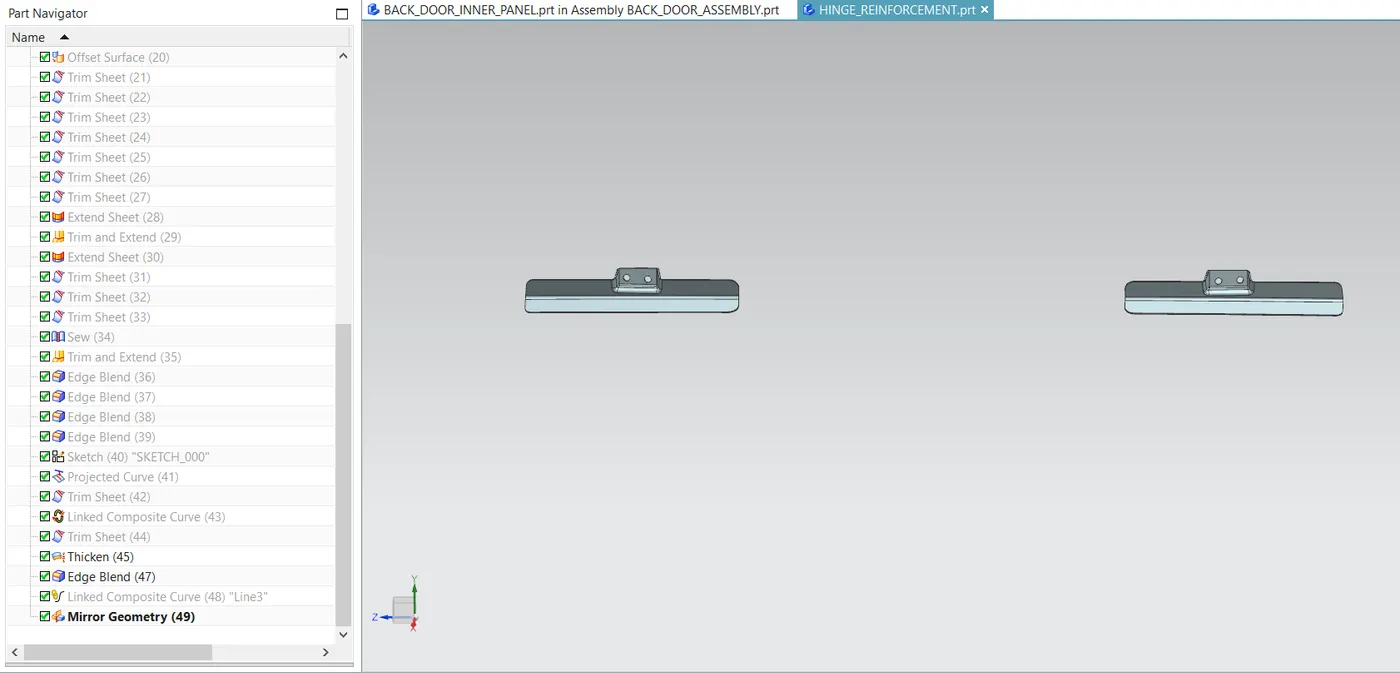
- Hinges enable the opening and closing of the back door. One end of the hinge is fixed on the backdoor and the other end on the Roof, on both sides. Hinges can be placed outside or inside the backdoor. Hinge reinforcements are added in this region to compensate for the weak zone developed due to the load acting while opening and closing the backdoor. Embossing is provided at the Hinge mounting area to compensate for the functional holes punched.
Gas Stay Reinforcement:
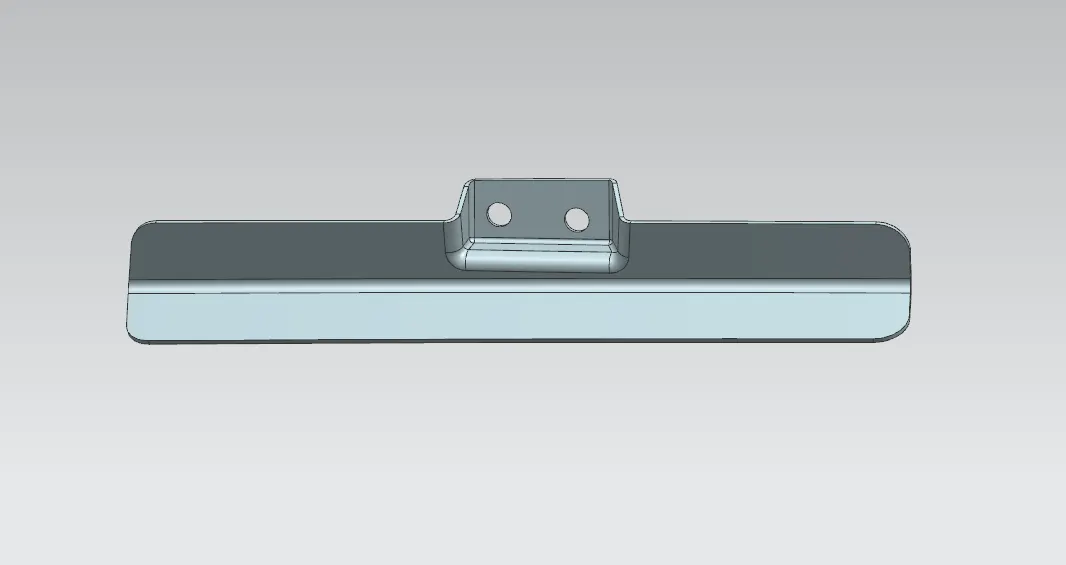
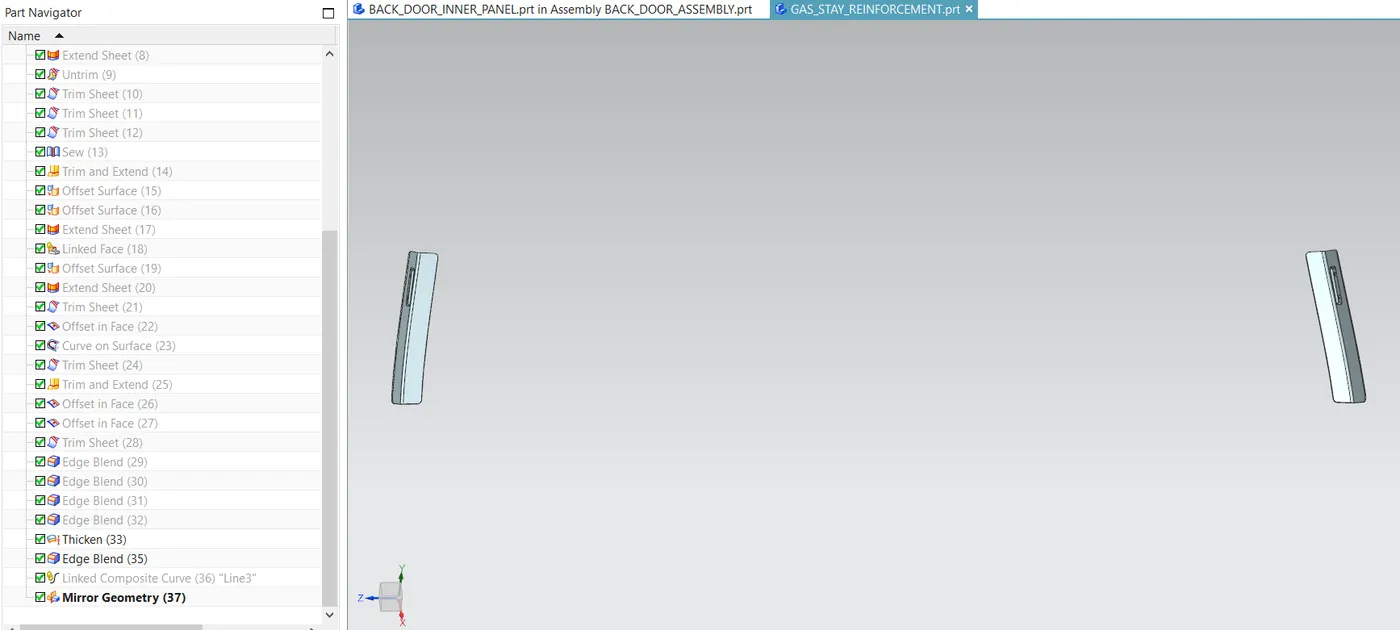
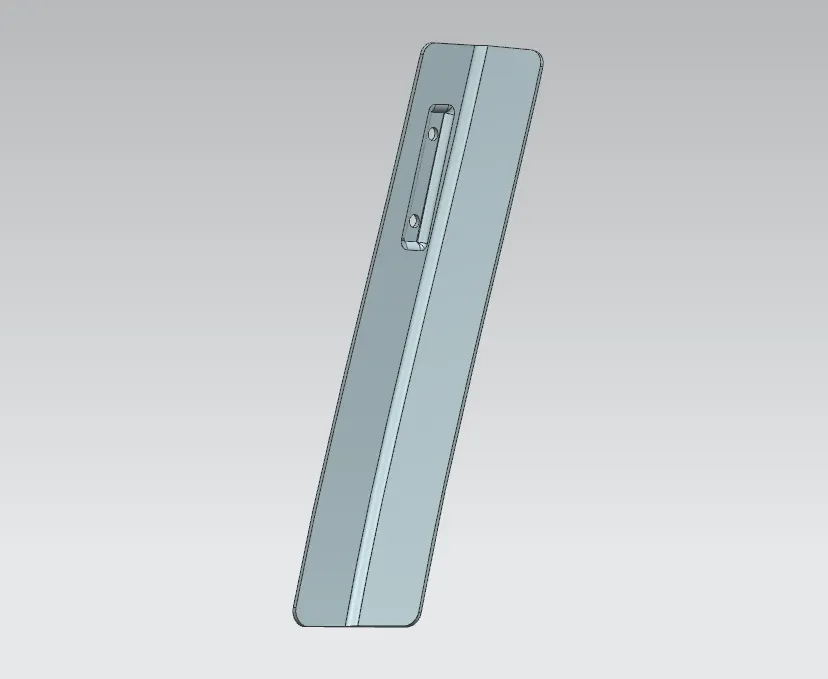
- Gas Stay is a device used for supporting the back door in its open position. Gas stay requires no manpower and is engaged into a support position automatically as the back door opens. One end of the Gas Stay is fixed on the backdoor and the other end is on the Body Side or on the Back door stationary area. Embossing is provided at the Gas Stay mounting area to compensate for the functional holes punched.
- Various simulation tests like the Bend test, Torsion test, and Abuse test performed on the back door as shown above reveal that there a very weak zone developed at the Gas stay region. To compensate for that, a reinforcement is added in that region.
Wiper motor reinforcement:
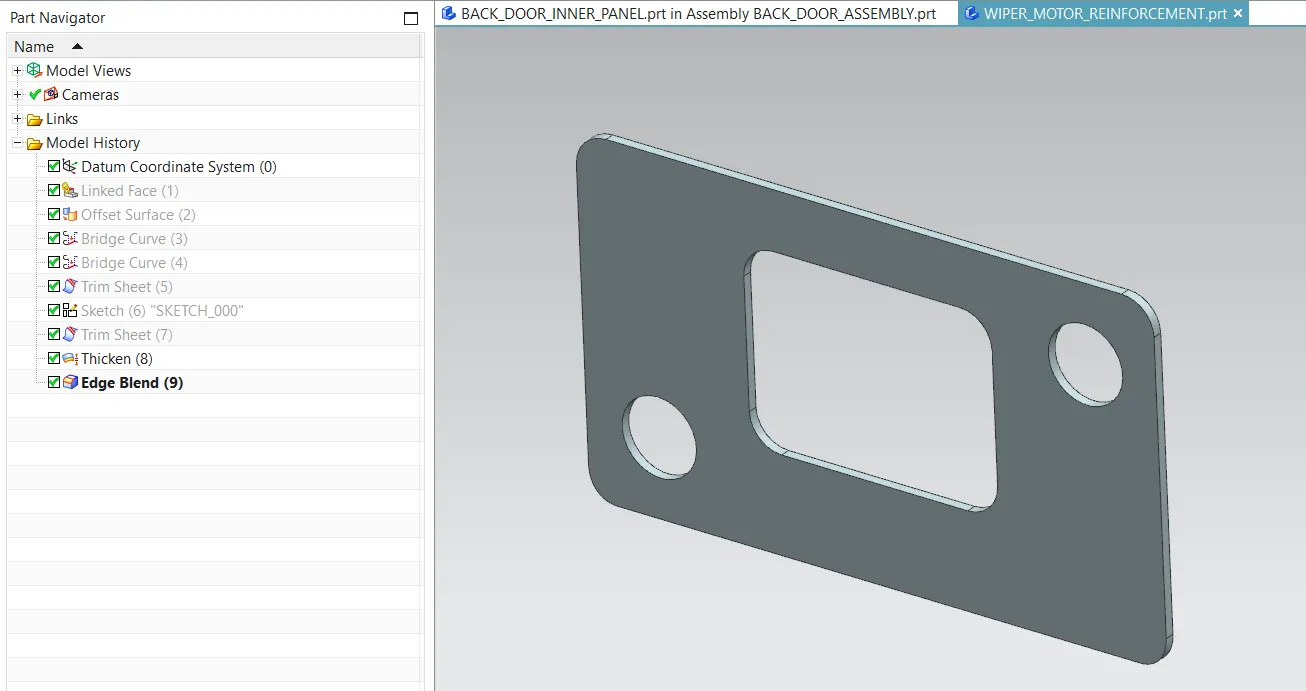
- Wiper Motor Reinforcement is created to mount the Wiper Motor Assembly.
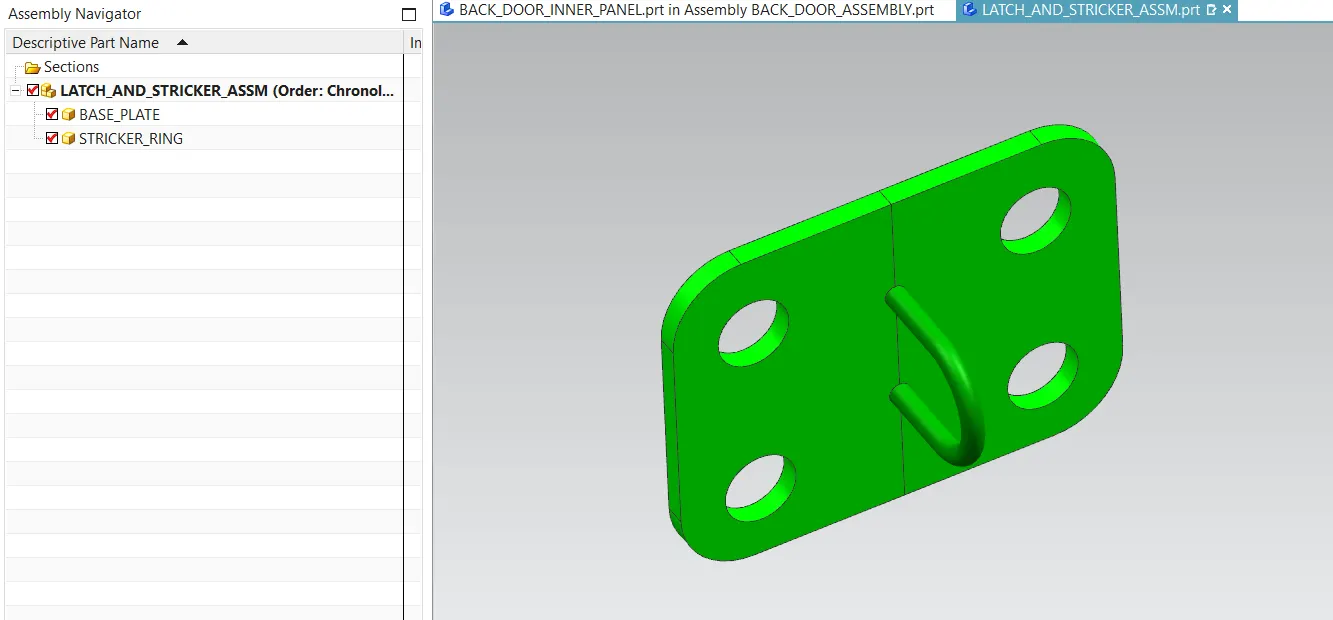
Latch and striker reinforcement:
- The Latch & Striker forms the locking mechanism of the backdoor with the car. Due to regular opening, closing, and over-slamming of the backdoor, there is stress developed in the Latch and Striker area. Further, during a rear collision this area will be the first point of contact. To compensate for the same, reinforcements are added in this area.
Reinforcement Assembly:
- The inner panel accommodates the Latch and Striker, Wiper Motor, Trims Mounting, Hinge, and Gas Stay, etc and therefore the necessary cutouts are provided. Various reinforcements are also spot-welded to the inner panel.
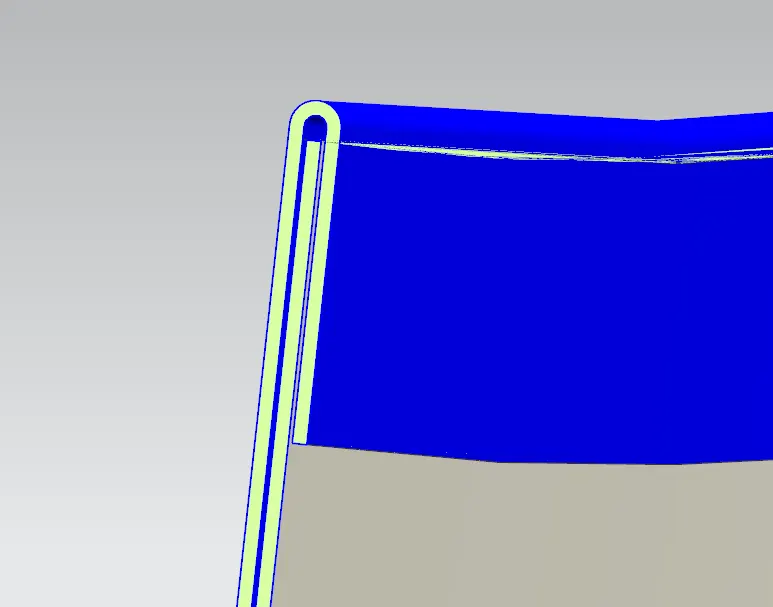
Hemming:
Hemming is the process of wrapping the flange of the outer panel to the flange of the inner panel so that they fit rigidly. After the hemming process, the sealants were applied along the edge of the flange of the outer panel so that water tightness was achieved. The below image shows the cross-section of the inner and outer panels joined by the hemming process.
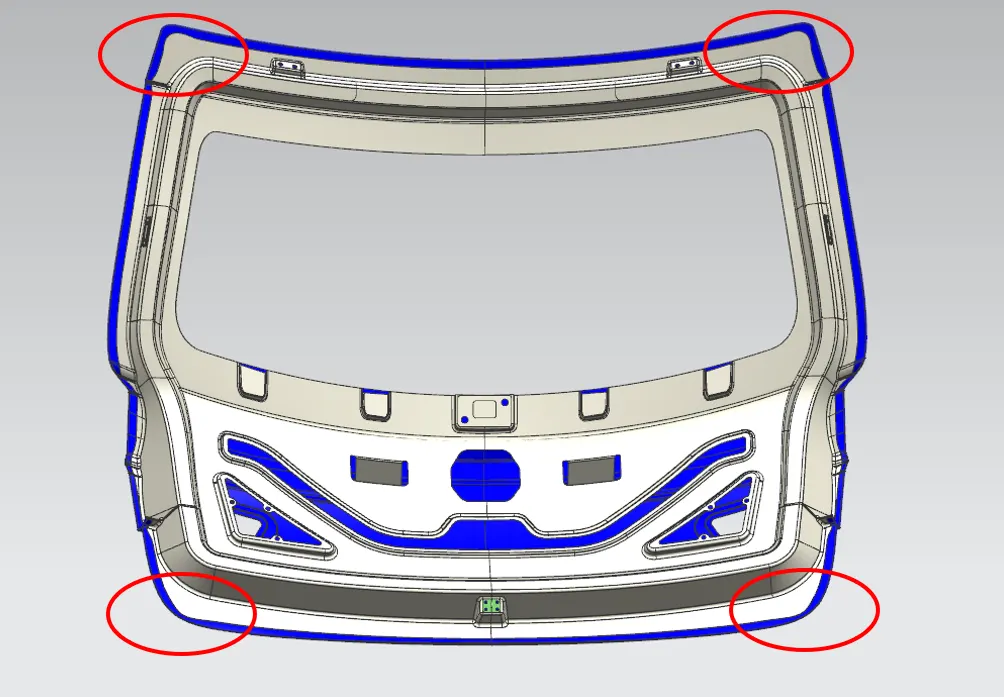
Usually, the reliefs were provided at the corners of the hemming flange to avoid the Hemming relief to avoid stress developed while hemming. stress developed during the hemming process.
Mastic Sealants:
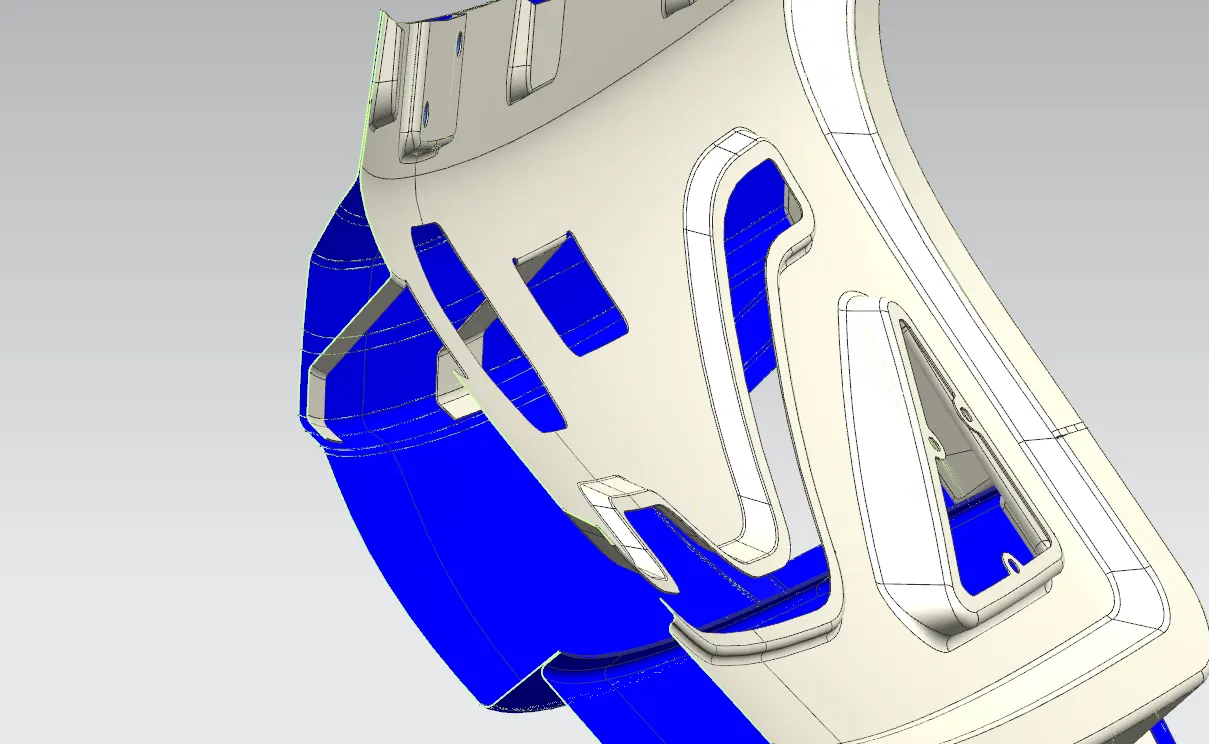
- To improve NVH (Noise, Vibration and Harshness) i.e to reduce these levels. Mastic Sealants are used. They also improves the strength. They are made of hard Rubber and are introduced as a paste thereby joining the inner and outer panel with a thickness of 5mm. Mastic Sealants are preferred over Spot Welding to join the inner and outer panel due to the fact that the latter reduces the aesthetics of the car, especially on the outer panel which is the styling surface.
Draft Analysis:
- While designing a component a design engineer must make sure that the component can produced by any means of manufacturing methods with the least amount of time, material, manpower, and power. So that we can reduce the overall cost of car.
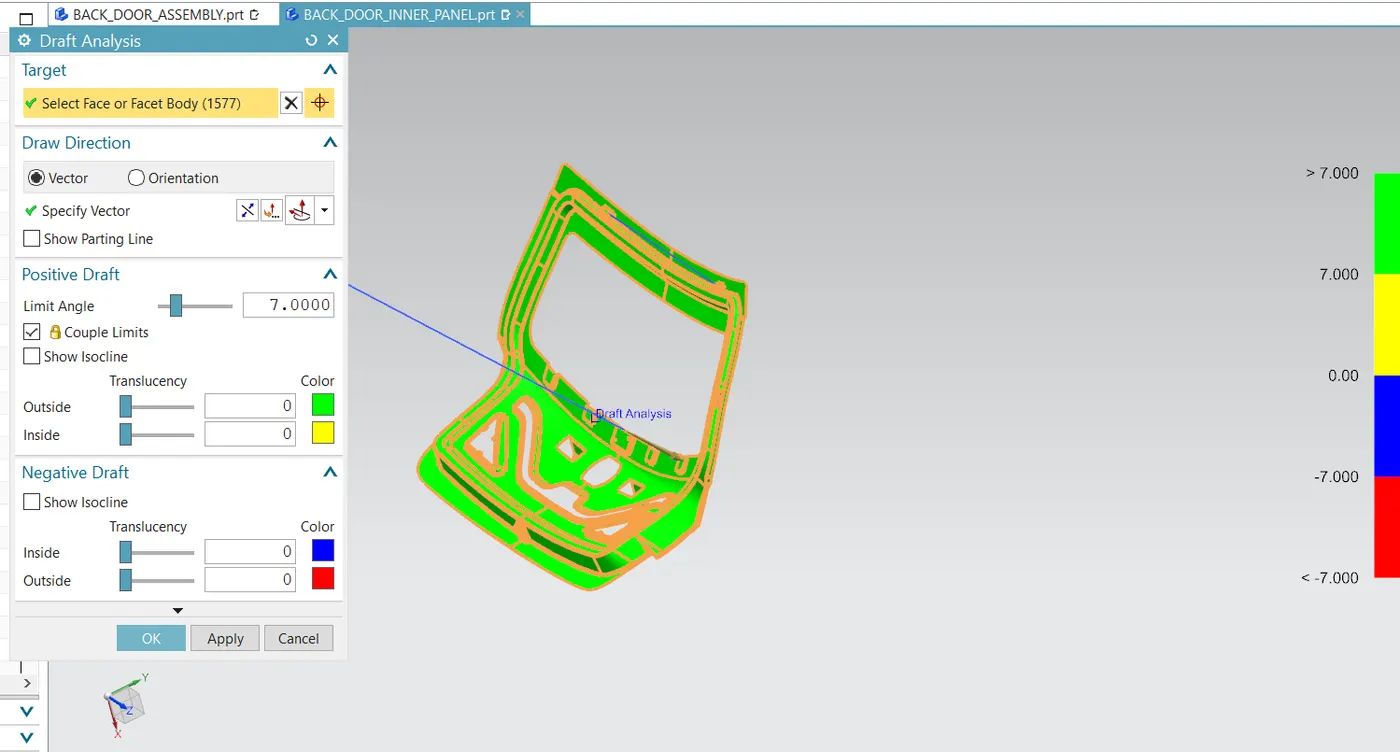
- When the Back Door is considered it is manufactured by deep drawing at most of the time Deep drawing is the process where a single sheet of metal is placed over a die that has the desired shape of the final output and the sheet is pressed against it with a tool. For the tool to come out from the part usually pressing relief of 5° to 9° will be provided during modeling itself.
- In NX draft analysis can be done after modeling so that we can verify whether the product is manufactured by pressing or not. One side of the surface is highlighted by green and other side by Red colour means that the model can be manufactured. Result of the draft analysis is shown in the figure below.
Conclusion:
Thus the Back door was designed and developed from the given styling surface with essential Reinforcements and Emboss. To satisfies the manufacturing requirements Draft analysis was also done on the Inner Panel.
Google drive Link: https://drive.google.com/drive/folders/1ZdKDJArqXn1p1x6EFRH981cKF9bx9IKB?usp=sharing