Design of backdoor
Aim: Design a Backdoor with given class A with all design standards.
Introduction:
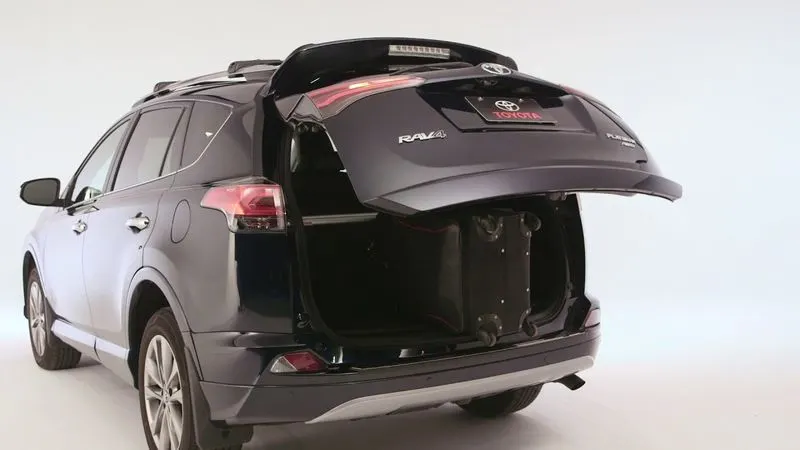
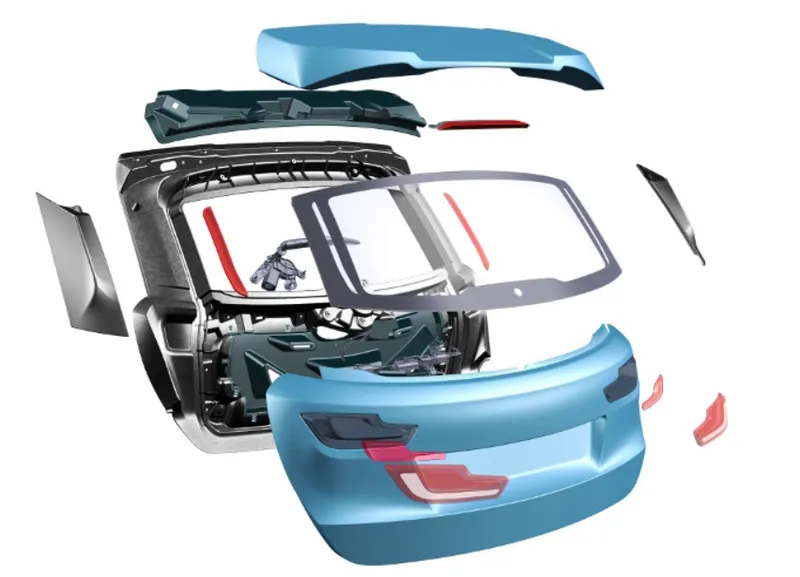
It is a hinged board or door that may be raised or lowered to facilitate loading and unloading.
Other names for the back door include "Hatch," "Tailgate," "Trunk-lid," and "Boot-door." It is the area of the car closest to the back that has mounts for the taillights, hinges, wiper motor, petrol stay, etc.
Uses for the Backdoor
- It safeguards against damage to the passenger's belongings and luggage.
- It houses the tail lamp assembly, the wiper motor, and other parts.
- It acts as a point of entry and exit for passengers and luggage.
- It has windscreen glass, which improves visibility from behind.
- It has parking sensors and a rearview camera attached.
Types of Backdoor
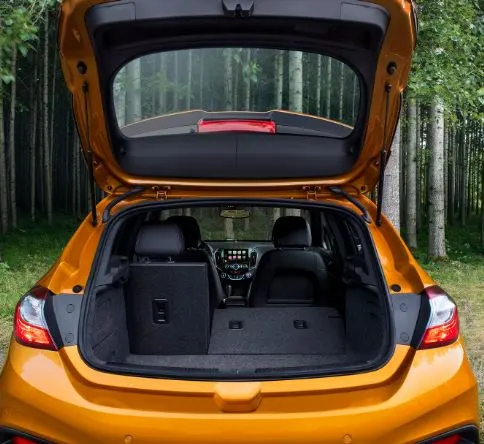
- Top mounted
These types of back doors are used in station wagons, pickup trucks, and some other sports utility vehicles.
- Side mounted
Typically Van-type MPVs, SUVs, and pickup trucks employ it. Compared to top-mounted ones, these side-mounted doors and barn doors are much simpler.
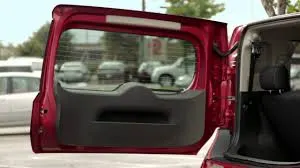
- Bottom mounted
Bottom-mount doors are used in estate-type cars, pickup trucks, and some luxury SUVs.
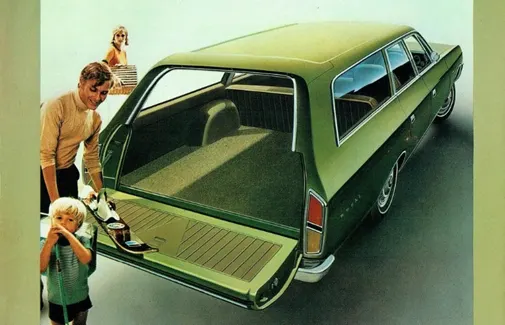
Material Selection:
The back door's overall weight is significantly influenced by the material choice. Steel and aluminum are the most often utilized materials. Because steel has a denser composition than aluminum, the door is heavier. The backdoor's construction material is determined by the car's budget; most low-cost cars utilize steel because it is less expensive than aluminum. Another thing to keep in mind is that using cast aluminum parts rather than deep-drawn steel parts eliminates the need for reinforcements and reduces the car's overall weight by about 5 to 10 kg, improving performance.
Components to be designed:
- Outer Panel
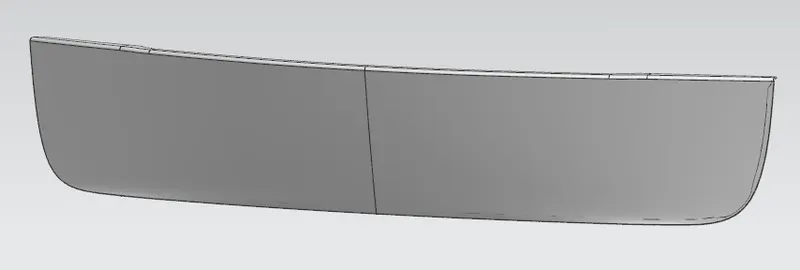
It is the back door's outside styling skin surface. It features multistage coatings that provide properties like scratch resistance and corrosion avoidance. Through the process of hemming, it is wrapped around the inside panel.
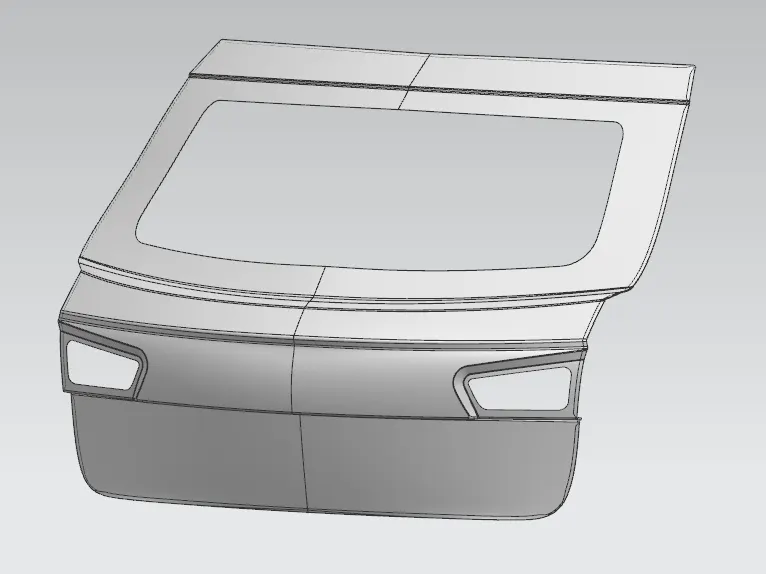
Outer Panel Upper:
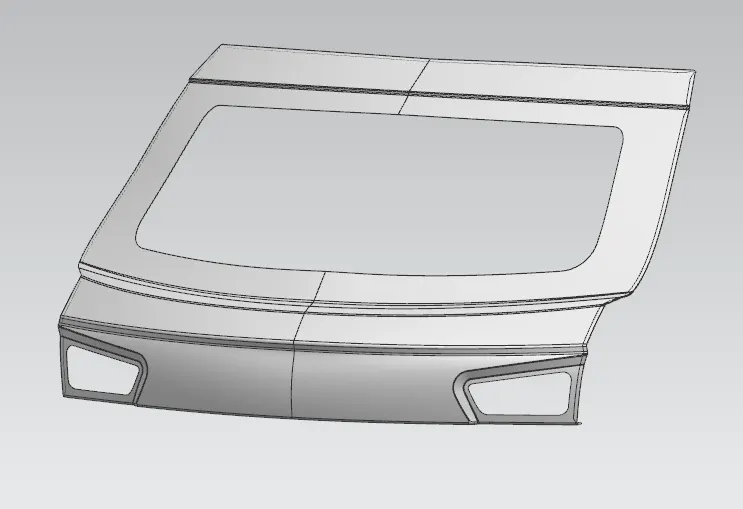
Outer Panel Lower:
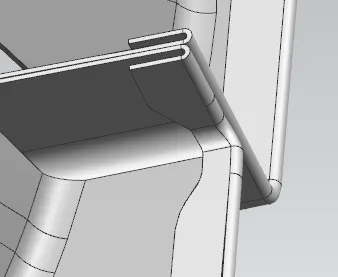
Hemming:
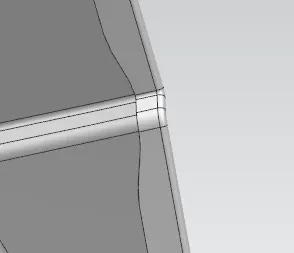
Hemming is a shaping procedure in which the sheet's edges are folded over another portion to create a snug fit. Hemming procedures are typically used to join components together, enhance a part's appearance, and reinforce part edges. Hemming is a secondary technique used in the assembly of automotive parts to link two sheet metal sections (the outer and inner) together after deep drawing, trimming, and flanging operations. For this kind of assembly, hoods, doors, trunk lids, and fenders are typical components.
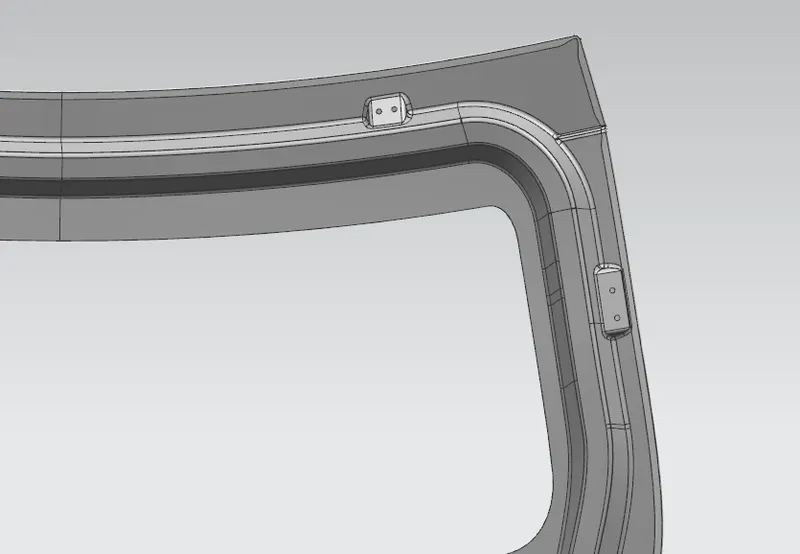
Corner Relief:
Because of the vibrations and stress concentrations caused by the many rollers used during the hemming process, the panel's original design intent shouldn't be altered. (i.e the panel should spring back to its original formation after the roller is removed). Reliefs are offered at corners to prevent this situation, however, most of the time that isn't the case there.
- Inner Panel
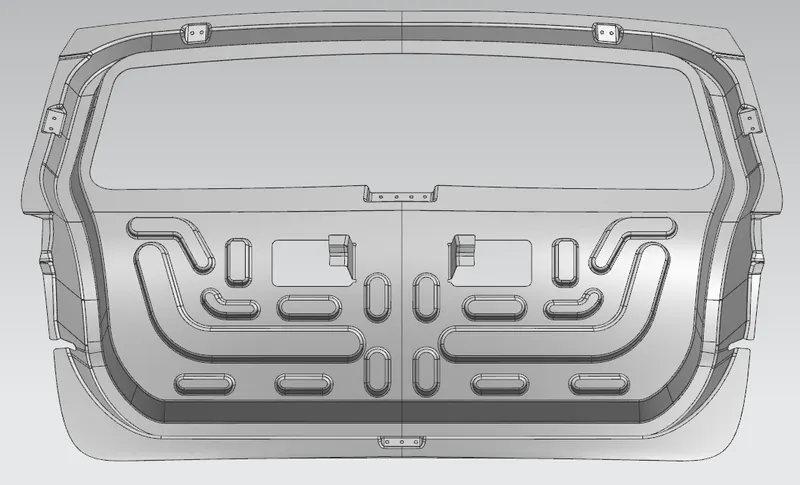
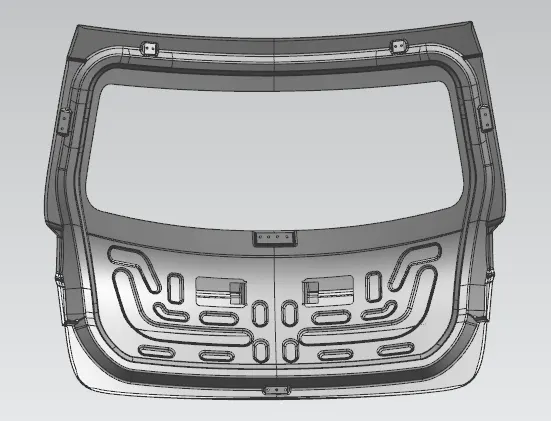
One of the most crucial part of the backdoor assembly is the inner panel. With the aid of the embossed patterns on it, it offers strength and aids in the absorption of external pressures. It assists in mounting accessories like hinges, wiper motors, gas stays, latches, and strikers, among others.
The inner panel is made either through casting or deep drawing. Most aluminum parts are cast, whereas deep drawing is used to create the steel inner panels. There must be a tooling direction via which that panel must be deep drawn if such is the case.
Tooling Direction:
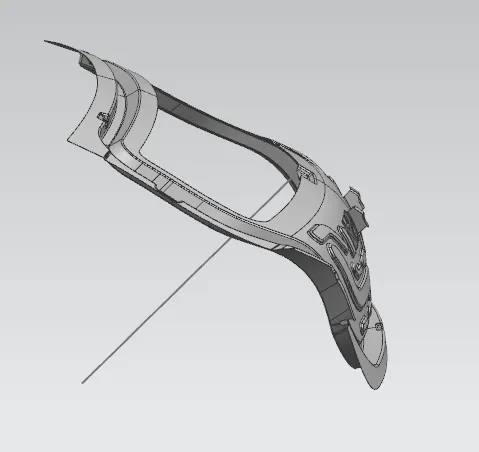
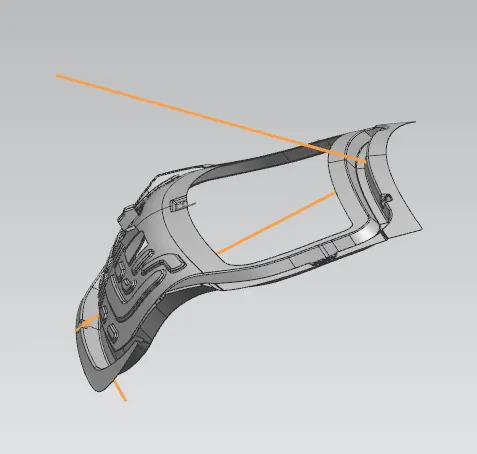
It is basically the direction in which the mold pulls apart. The mold is built in two separate pieces, basically. You have a Cavity side and you have the Core side. The Core pulls apart from the Cavity and that's the Dyeline or the Tooling Direction.
Embosses:
They are offered to provide sheet metal panels more strength and to aid in channeling forces and energy in a particular direction.
Mastic Sealants:
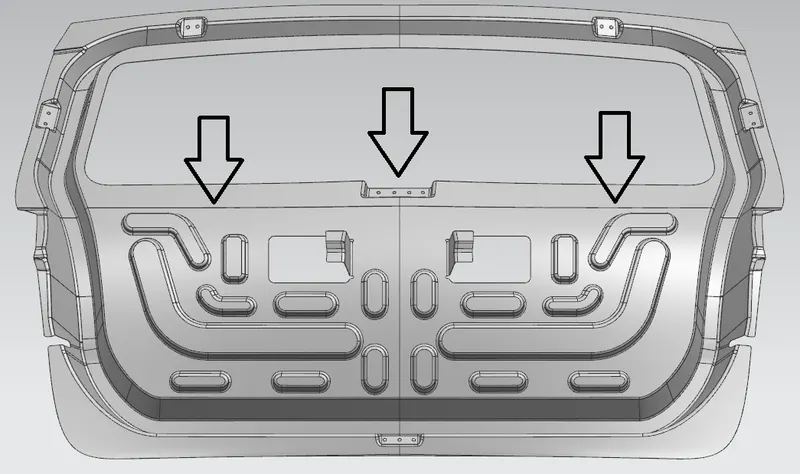
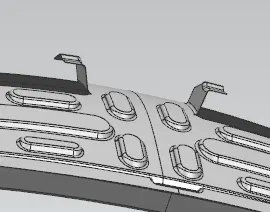
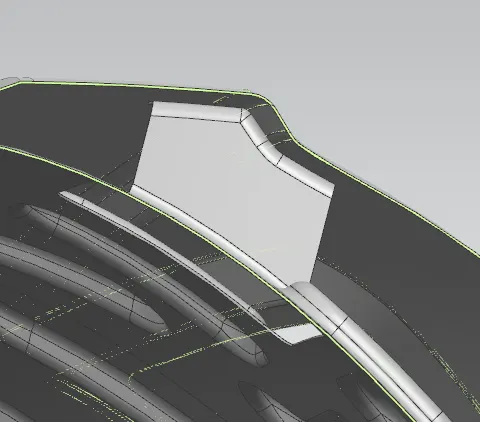
Since the outer panel contributes to the vehicle's aesthetic appearance, we cannot join parts using bolts, spot welding, or any other method that detracts from the panel's aesthetic appearance. Mastic sealants are thus employed to bond the inner and outer panel parts. The distance between places where mastics are to be applied must not be less than 5 mm.
These flanges help to attach the outer and interior panels by placing mastic sealant there.
Reinforcements:
In order to preserve the rigidity of the panel assembly, reinforcements are typically installed to increase the strength of the panel in certain localized locations that are relatively tiny compared to sheet metal sections for absorbing loads imparted thereon and dissipating such loads throughout the panel assembly. The panel used in this section is 0.75mm thick, whereas the reinforcements are typically 1-1.5mm thick.
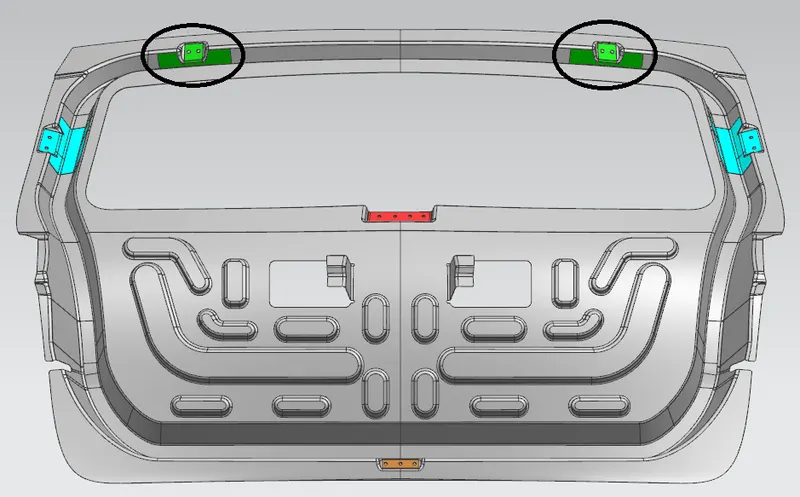
- Hinge Reinforcement:
The backdoor's whole weight is supported by the hinge, a pivoting device. As a result, reinforcements are added for rigidity and strength.
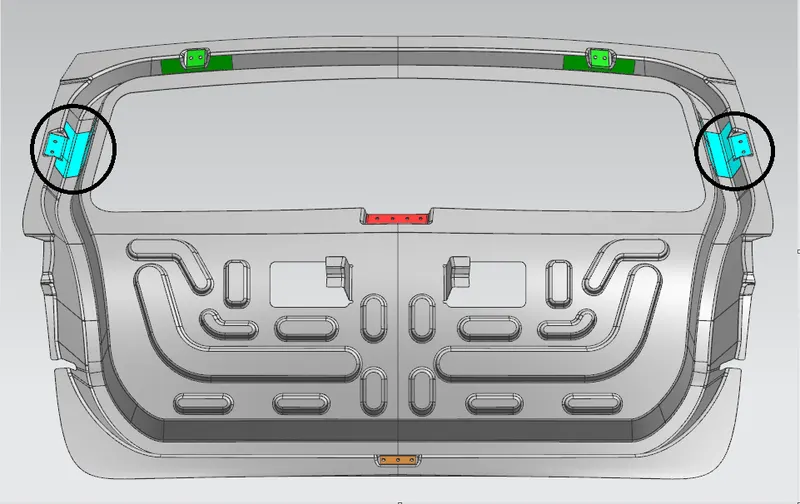
- Gas Stay Reinforcement:
The backdoor is raised automatically by a gas stay, which also serves to support the backdoor while it is open. It comes in two varieties. both partially and entirely automated.\
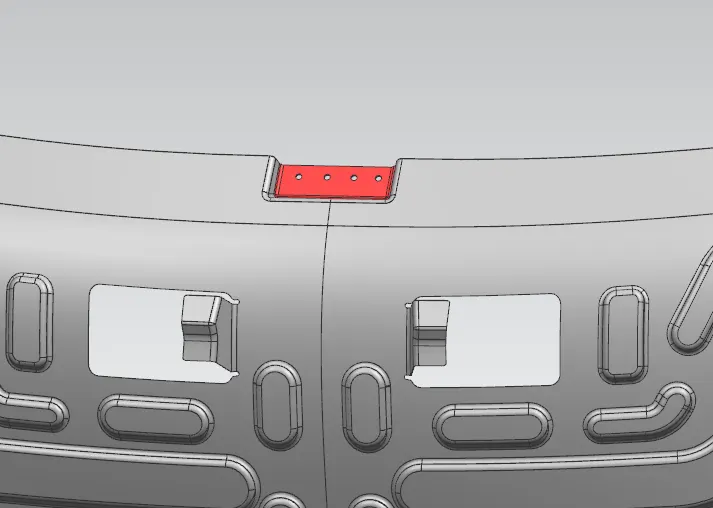
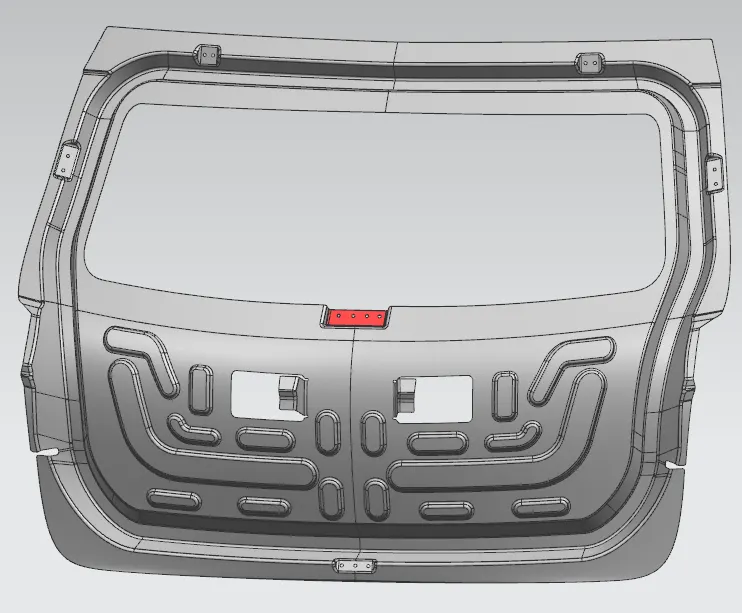
- Wiper Motor Reinforcement:
The rear visibility is affected by dust and wetness on the windshield, which is removed with a wiper. The motor, which is located on the interior panel, operates it. The inner panel becomes distorted as a result of the motor's vibration and heat, which reduces the panel's strength and stiffness and causes poor noise, vibration, and harshness (NVH). In order to prevent these circumstances, reinforcement is given.
- Latch and Striker reinforcement:
For the placement of the latch and striker assembly, an emboss is made in the bottom portion of the panel. The door is being opened and closed abusively and repeatedly, necessitating the installation of reinforcing.
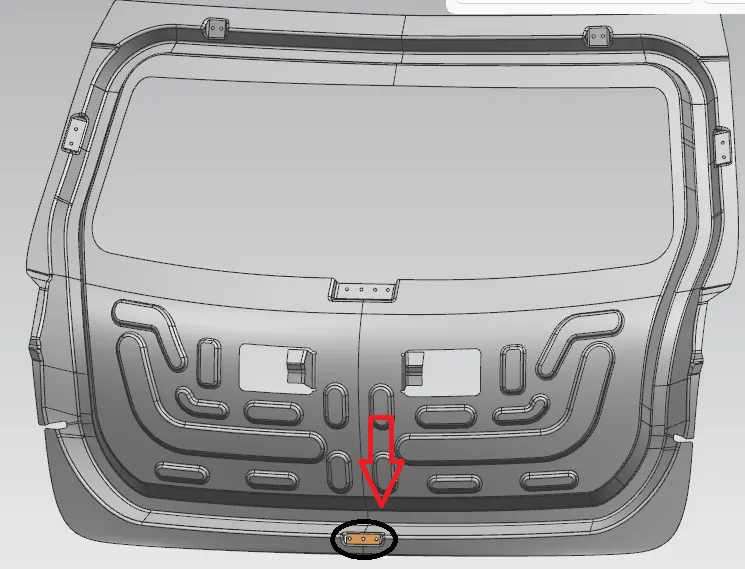
- Positioning of Latch & striker/ Latch Trajectory:
The backdoor's swinging portion revolves around the hinge axis. For the backdoor to open and close correctly, the latch striker's position and orientation are crucial. The striker is passed through at the proper location in relation to the inner panel by a circle whose center serves as the hinge's axis.
Design Considerations:
- Rear visibility
- Accessibility and boot space
- Filtering Flange
- Supporting elements such as hinges and gas stays.
- Wiper motor, taillight, and other wiring loops mounting brackets
- Joining methods include spot welding, hemming, etc.
Assembly:
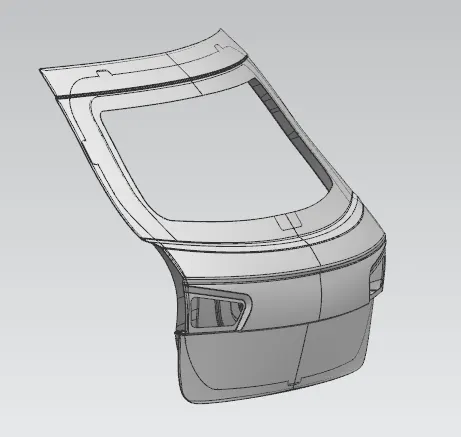
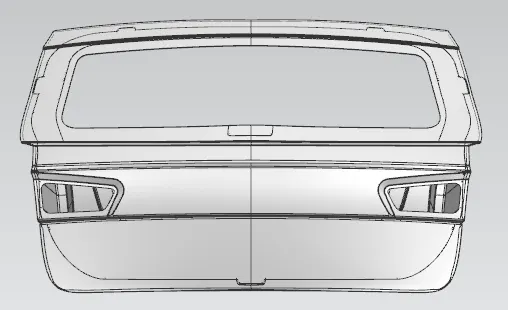
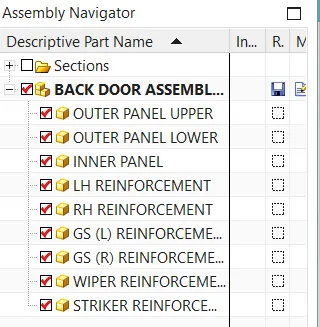
The inner panel of this assembly was made first according to design inputs & considerations. Then, one by one, the additional parts were modeled in accordance with the inner panel specifications.
Draft Analysis:
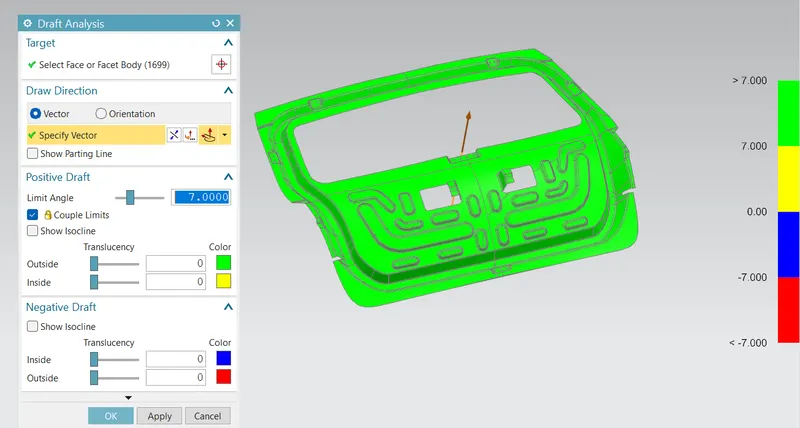
Every component made with a press tool or another type of forming tool needs some positive draft on the faces that are perpendicular to the tooling direction. On these faces, if we don't provide any draft (zero draft) or provide any negative drafts, the material will stick to the surface of the mould and, when the mould is in motion, it will obliterate the surface, lowering the surface finish. Therefore, using the Draft Analysis command, we can determine whether or not the component we have drafted can be easily expelled. Additionally, it provides information on the crucial zones, allowing for any necessary design modifications. In our case, it is all clear with a minimum 7-degree draft.