Design of backdoor
AIM:
To design the back door of the car and make the inner panel for the back door and also design the necessary mounting prats like latch and striker reinforcement, hinge reinforcement, wiper reinforcement, gas stay reinforcement
Introduction of back door\tail gate:-
A door is a hinged part which is used for entry and exit of the vehicles. Back doors are one of the type doors of the vehicle le which are located next to the passenger seat which provides access to the luggage compartment. In most of the cars, these back doors are operated with the help of gas stay which in turn reduces the effort required to lift open the door. Some luxury cars have powered backdoor which in turn is driven by an electric motor. This kind of system is also called a powered trunk lid system. Hatchback or station wagons are sold as 3 door or 5 door models. In this case, the rear hatch is classified as door this is because it enters the passenger compartment. The naming is mainly used in Europe countries. In case of safety, the back door designed should meet the safety requirement for the rear collision.
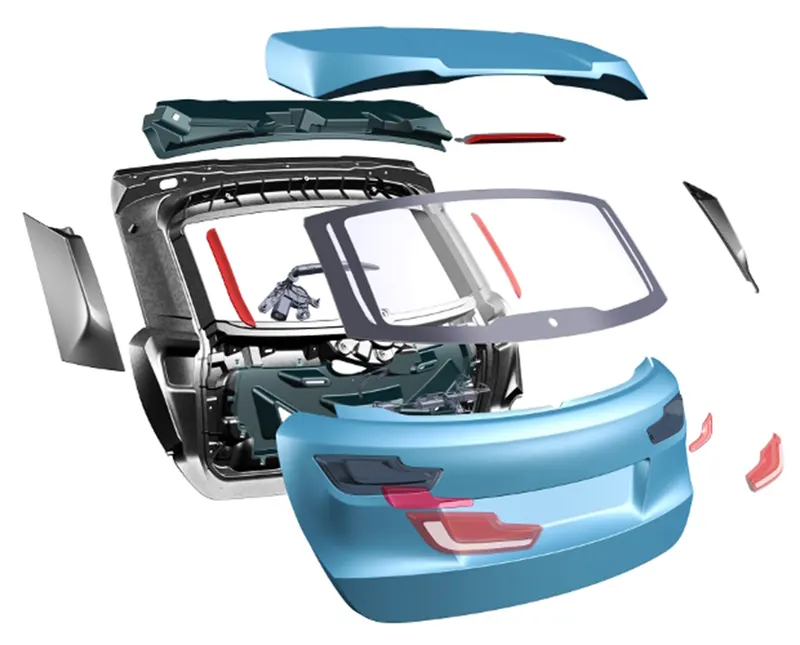
A backdoor is located at the rear end of the car which gives access for the boot space to store luggage, spare wheel etc. These doors cab be operated manually or electric powered. In most of the luxury car is electric powered. Back door is also called as 'Hatch' or 'tailgate', 'trunk-lid', 'boot-door' is basically the 5 door in a 4-door car. Its rearmost part of the vehicle which gives access to the trunk and has mounts wiper motor, tail lamps, hinges for supporting its weight in opened position, gas stay which help with its opening and keeping it open, radars and cameras etc.
A backdoor is usually made up of 1 inner panel and 2 or 3 outer panels joined together by hemming and spot welding wherever necessary. The material used for backdoor varies as per the price range of the vehicle. Most of the low cost vehicle use steel as it is cheaper and use parts are stamped using moulds. These parts are usually of uniform thickness and reinforcement are added to improve local strength where needed.
A, Types of the back door based on working positions.
The door or opening of a cargo area may be hinged at the top, side, & bottom. If the door hinged in the bottom it is called as a tailgate.
1.Top-mounted:
This type of back doors is used in a station wagon, pickup truck and some of the sport utility vehicles
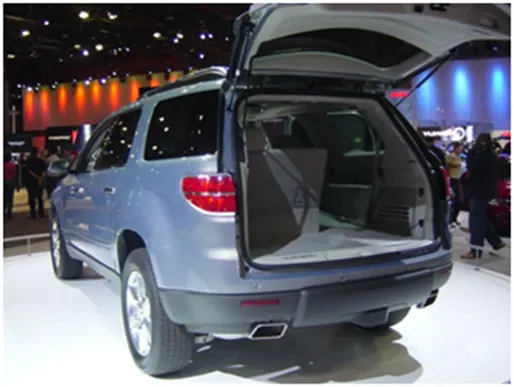
Today’s modern cars use top-mounted tailgating systems which are both powered and also gas stay supported. These top mounted tailgates provide greater rear visibility compared to side-mounted or bar doors which have canter pillars in it.
2.SIDE MOUNTED DOORS:
As the name signifies side-mounted doors are the one which is used in the van type MPVs, SUVs, pickup truck vehicles. These side-mounted doors or barn doors are a lot easier compared to top-mounted doors.
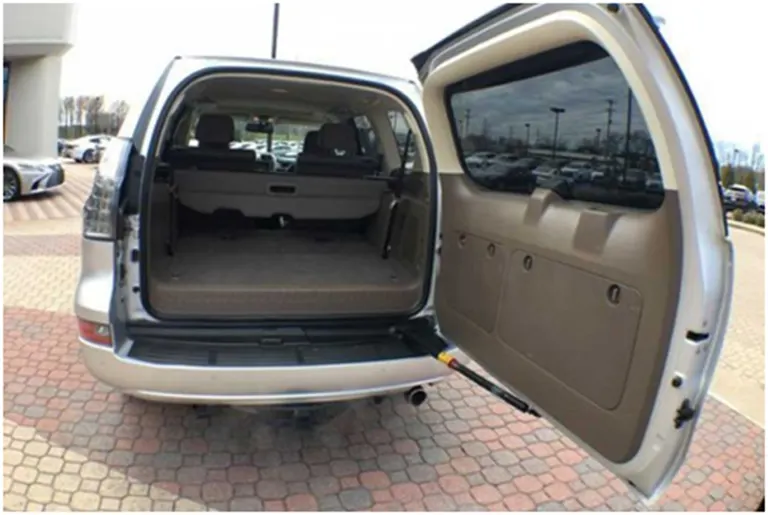
These doors are generally smaller in size and can be easily accessed. These doors are more convenient for the goods handlers for long pipe and lengthy components where one door is kept open. These doors also save accidental head impacts. It is a lot easier to load and unload items in the side-mounted doors.
3.Bottom / split type:
This bottom type or split type backdoor system are used in the car type such as estate type car, pickup trucks and some luxury SUVs.
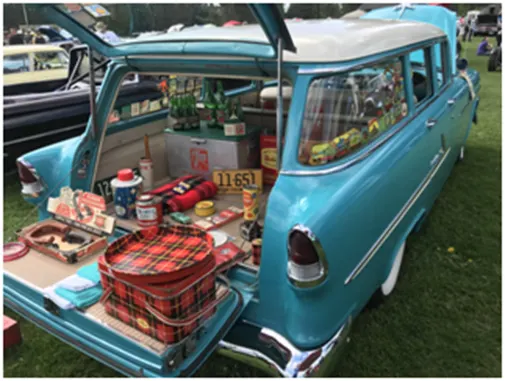
These are the most convenient type of back door in which the bottom split is used as a support or even as a table for the tour going people.
B.Types based on working mechanism.
1.Gas stays type:
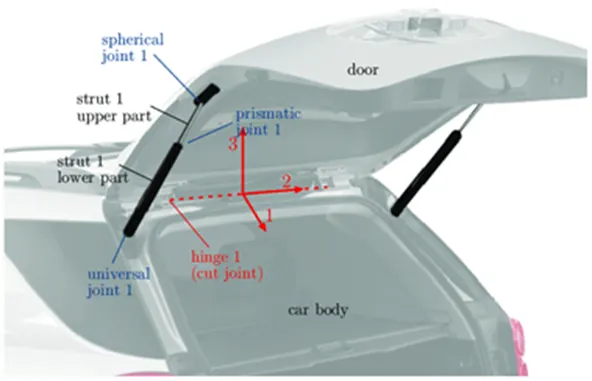
Gas stay types backdoor/liftgate/tailgate is an ideal and most commonly used tailgate mechanism from lower segment car to luxury car segment. The ideal components of tailgate consist of a hinge, door, gas stay and some rubber beadings for sealing of door which is shown in the image below:
2.Powered lift system:
Power trunk lid system is another sophisticated way of trunk/liftgate opening mechanism which is to automatically open and close of the trunk/liftgate and release of the latch by the touch of a button. The following image shows the component as used in the powered trunk/back door lift system.
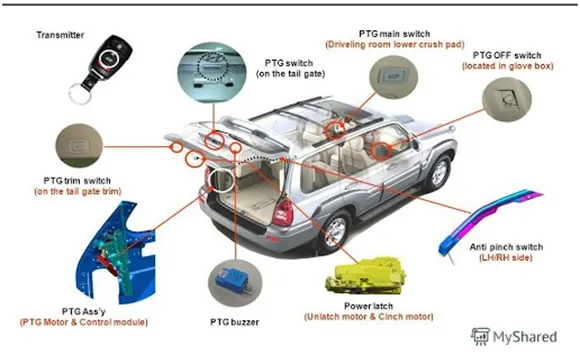
Powered trunk lift system consists of a power latch, anti-pinch switch, PTG ass’y, PTG main switch. When the switch is pressed in the compartment or outside the power latch releases the latch and the entire backdoor is opened. The anti-pinch switch is located in order to avoid accidental hand insertion during the operation of the door.
Materials Selection:
The selection of material plays a major role in determining the overall weight of the back door. The common materials used are Steel & Aluminum. The density of Steel is higher than Aluminum thus adding more weight to the door. The material used in the manufacturing of the backdoor depends upon the budget of the car, most low cost vehicles use steel as it is cheaper compared to Aluminium. Another aspect to be noted is that, if casted Aluminum parts are used instead of deep drawn steel parts there is no need of reinforcements and the overall weight of the car is reduced by approximately 5-10kg thus increasing the performance of the vehicle. Also the draft angle for casted parts is around 3 degrees while for deep drawn parts is around 7-10 degrees which helps in increasing the luggage/ cabin space.
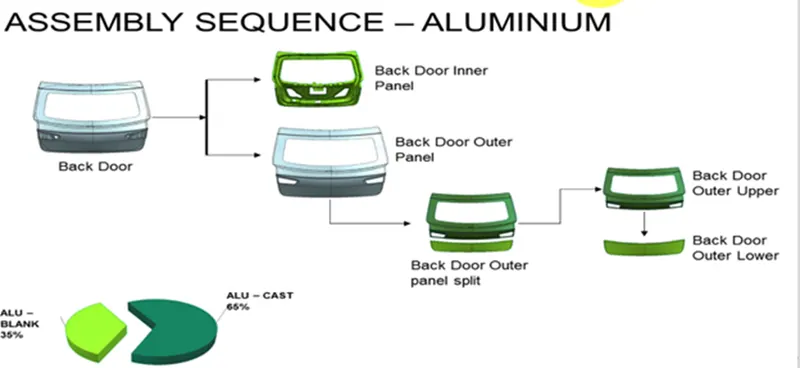
Figure. above shows possible no. of parts in aluminum(AL) backdoor
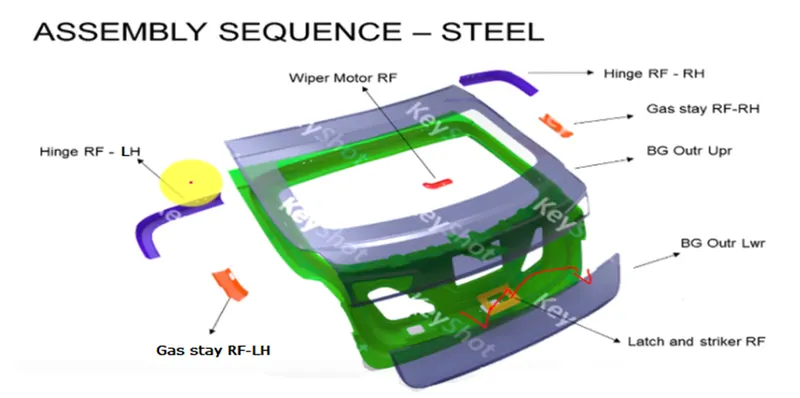
Figure . above shows possible no. of parts in Steel backdoor
The below table gives a comparative information about Steel and Aluminum.
|
Aluminium |
Steel |
|
|
Parts |
Parts are casted |
Parts are stamped |
|
Reinforcements |
Reinforcements can be neglected |
Reinforcements are necessary |
|
Thickness |
Thickness can be varied |
Thickness should be uniform |
|
Weight |
Lighter in weight |
heavier in weight |
|
Cost |
Costly as compared to Steel |
Cheap as compared to Aluminium |
|
No. Of components |
Less No. of components |
More No. of components |
Different types of Sheetmetal operations are done in the Back Door
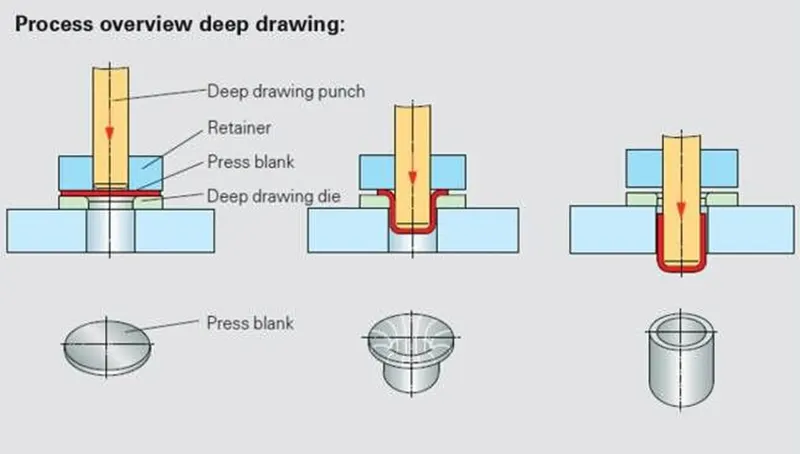
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
1.First- stage drawing:
The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head
2.Redrawing:
The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
Embossing:
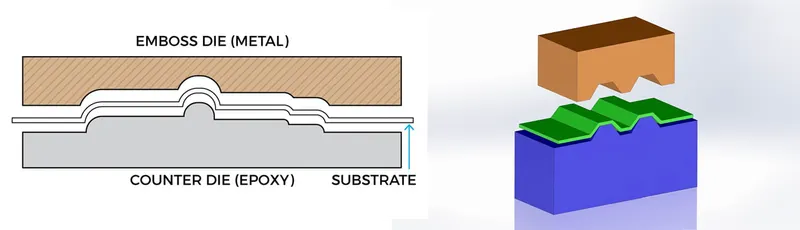
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
Hemming:
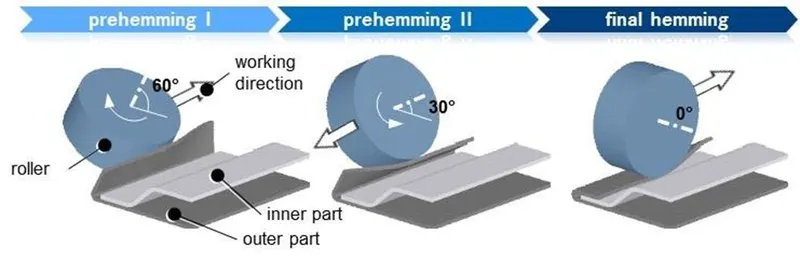
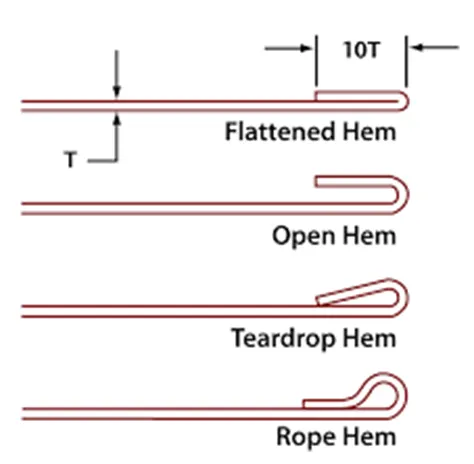
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
There are various types of hemming operations:
1.Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
2.Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
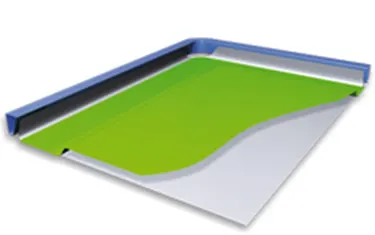
Open Hem: A Hem has a full round feature and a return flange. In open hem bend angle is equal to 180 degrees.
Tear drop Hem: In tear drop hem the bend angle is greater than 180 degrees.
Closed Hem: Hems without any inside radius are called as closed hem. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminum.
Blanking:
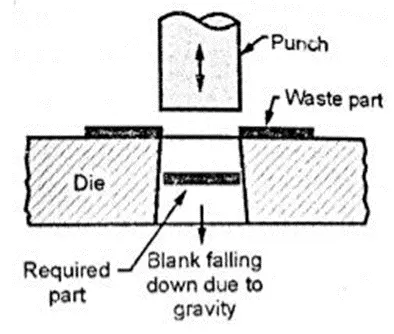
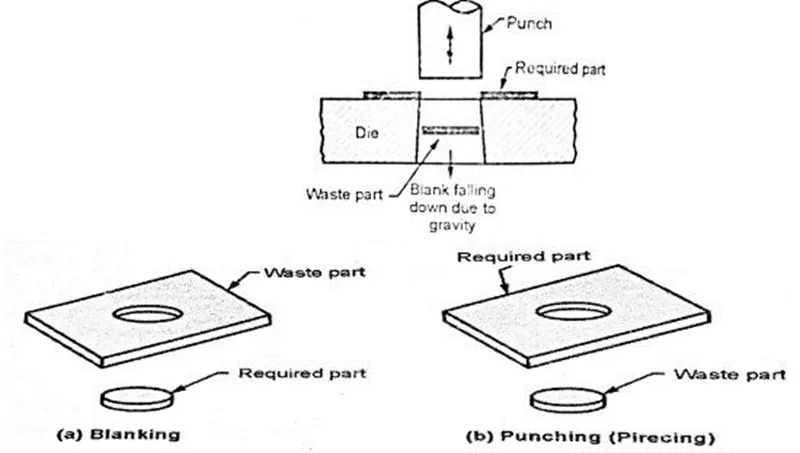
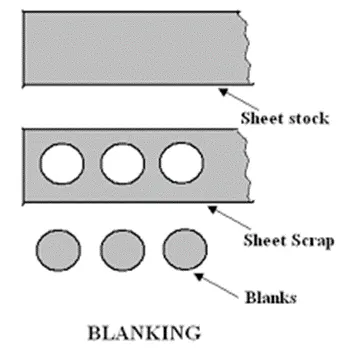
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered as a waste.
Punching:
It is similar to blanking only the main difference is that, the hole is the required product and the material punched out from the hole is considered as a waste.
Back door components
1 back door outer panel
- Back door inner panel
3.Latch reinforcement
- Gas stay reinforcement
- Wiper reinforcement
- Hinge reinforcement
Here, we I do above mentioned component in nx cad 12.0, and also consider manufacturing feasibly
With respect to tool direction,
inputs for designing of backdoor:
1.Outer Panel - 0.75 mm
2.Inner Panel - 0.75 mm
3.Reinforcements - 1.5 mm
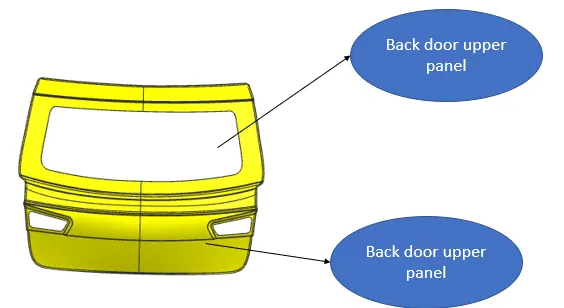
OUTTER PANEL UPPER AND LOWER:-
Outer panel is the styling surface of the back door. Glass for rear visibility is mounted on the outter panel upper. rear light are also mounted on the outter panel upper. Number plate is mounted on the outter panel lower. Spot welds and other manufacturing process should done only on the inner panel because the outter panel is styling surface which should not have any scratches or welds. Because it affects the style of the car which leads to bad impression on the customer.
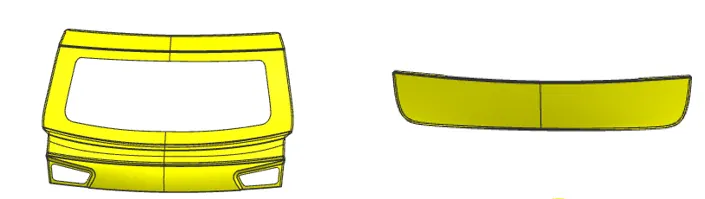
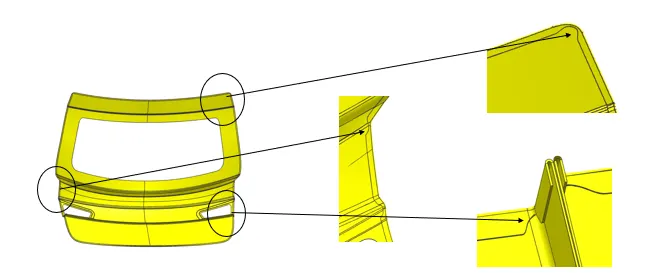
During manufacture feasibility ,corner relief provide in edge area,
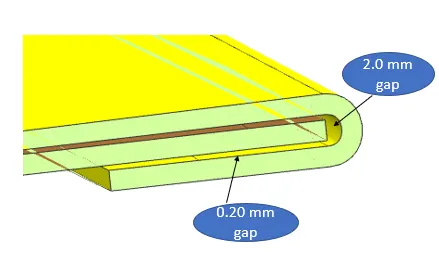
To do joint inner and outter panel ,we create sealt profile at list 4to 5mm gap and corner joint between the hemming operation
Mastic Sealment area,
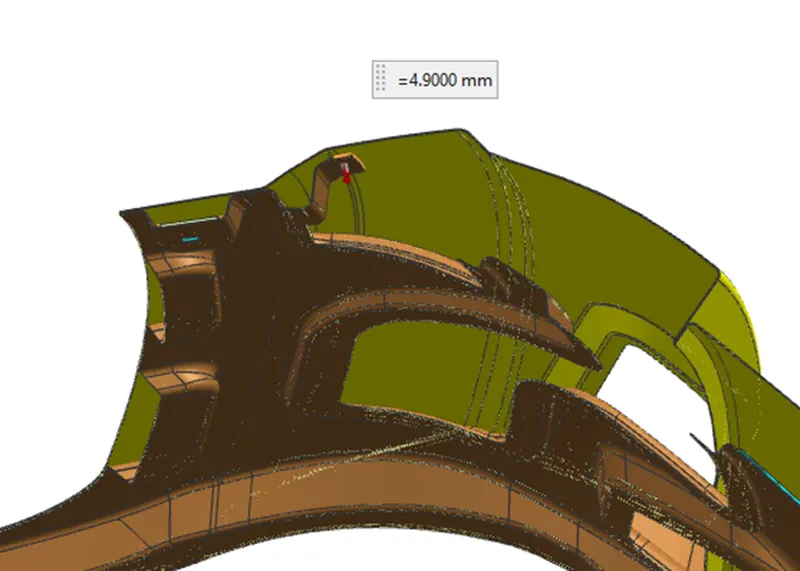
Hemming area,
INNER PANEL:-
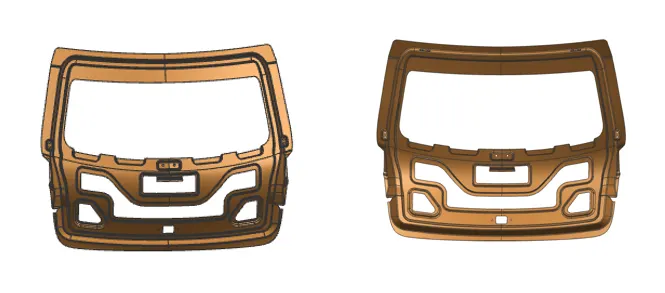
The inner door panel is a component which is used for strengthening the door assembly and it is one of the most important components on which all accessories are mounted like hinges, glass guide channel, moulded trim, latch etc. The possible method is the integration method. In the integration method, the part is stamped out of a single blank. This reduces the number of tools needed; the assembly cost and eliminates any fit ability problem.
Car backdoor inner panel is made of either steel or aluminium. Most of the luxury car's inner panel are made of aluminum because of its properties. But the cost of aluminum is high. Cost of aluminum is more as compared to steel. To easily understand, the cost of aluminum for inner panel is higher than the cost of all parts of backdoor together.
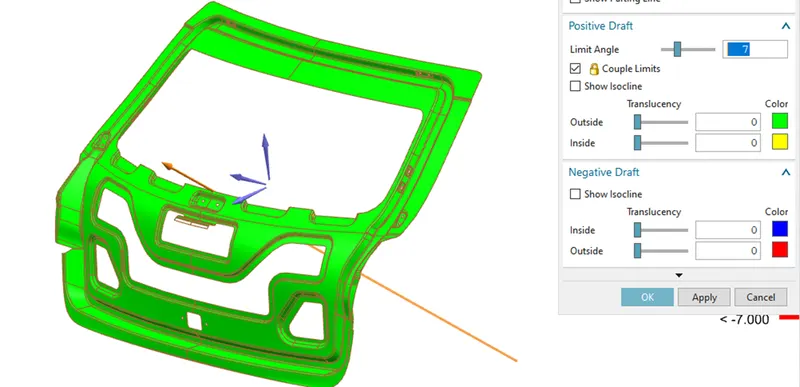
Draft analysis:-
draft analysis done for inner pannel,
HINGE REINFORCEMENT:-
What is a hinge mechanism?
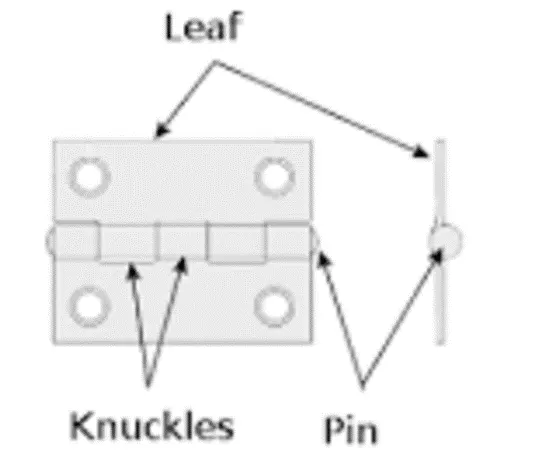
A hinge is a mechanical bearing that connects two solid objects, typically allowing only a limited angle of rotation between them.
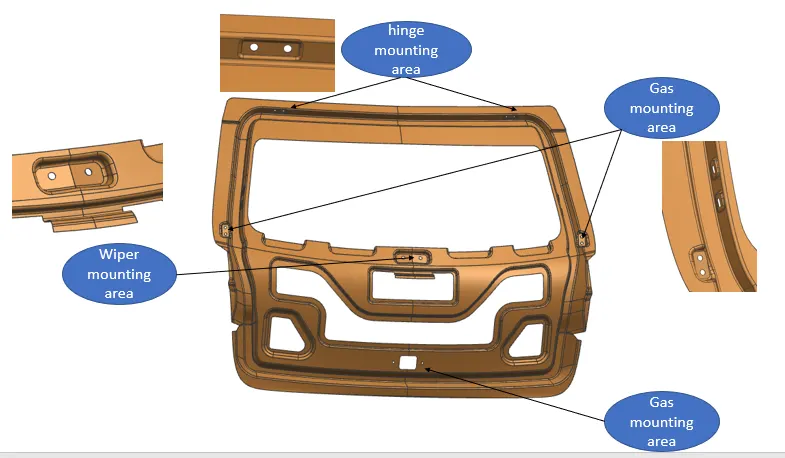
Hinges support the weight of the whole backdoor.Hence,the reinforcement must be provided there too.The emboss is designed in such a way that the hinge should operate freely.The hinge is connected to the rear roof of the car.
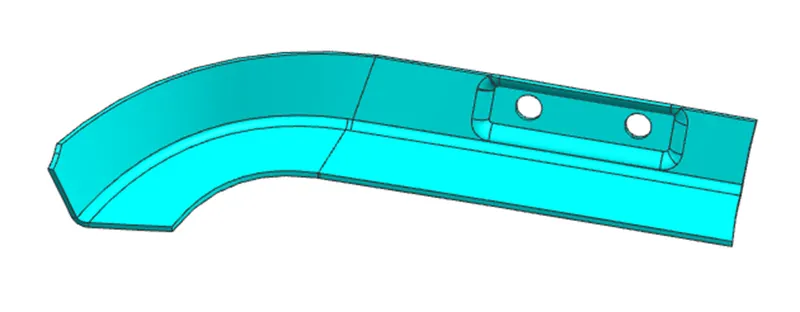
GAS STAY REINFORCEMENT:-
Gas stay reinforcement is used to lift the backdoor automatically.There are two types of gas stay one is semi-automated type the back door needs little force to lift after that it lift the backdoor automatically.In fully automated,it has power spindle which lift the bck door automatically.
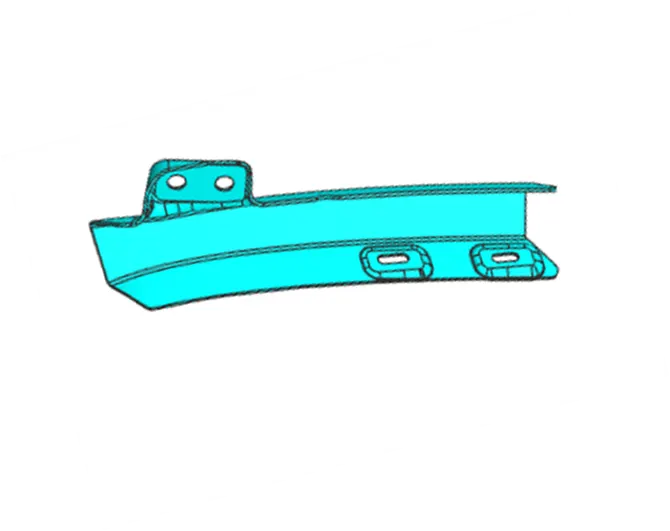
WIPER MOTOR REINFORCEMENT :-
Wiper is ued to to wipeout the rain water falls on the backdoor window.Its actuated by the motor which is mounted on the inner panel.Due to the vibration and heat created by the motor.The inner panel where the motor is mounted gets deform and parts attached to the motor starts to vibrate which leads to poor NVH.So we have to provide the reinforcement where the wiper motor is placed.
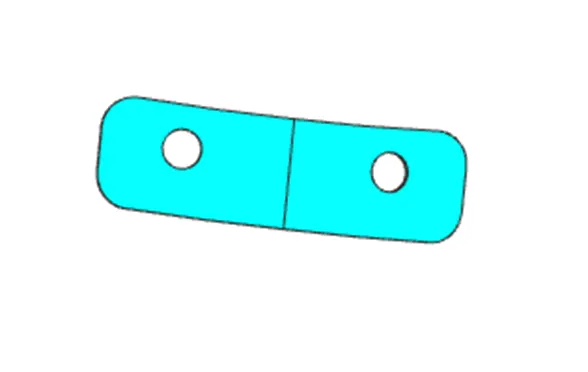
LATCH REINFORCEMENT :-
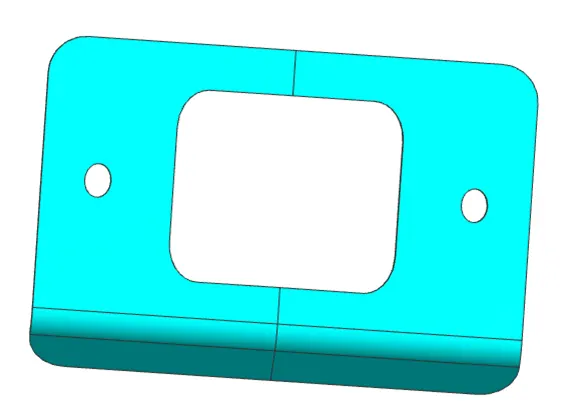
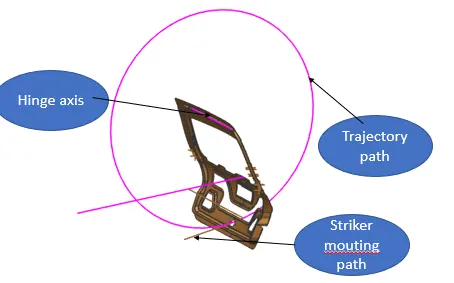
At bottom of the panel, reinforcement and emboss are given to accomodate the latch and striker assembly. Generally key operated or automatic remotly controllable mechanism is used to keep the door open or closed. The actuators,recivers and other electronics devices are mounted on the inner panel only.
Trajectory path for latch and striker :-
CONCLUSION
The back door outer and inner panel were designed with the help of the styling surface along the tooling direction and Draft analysis was performed on the inner panel and All the reinforcements were designed and placed at appropriate positions.