Week 9 - Project - Master Section Development
B PILLAR DESIGN THROUGH MASTER SECTION DEVELOPMENT
AIM :
The objective of this project to develop Closed Surface Model using Master Sections and to develop attachment features for Fixation of Parts by following OEM Design standards and procedures in CATIA SURFACE WORKBENCH and PART DESIGN
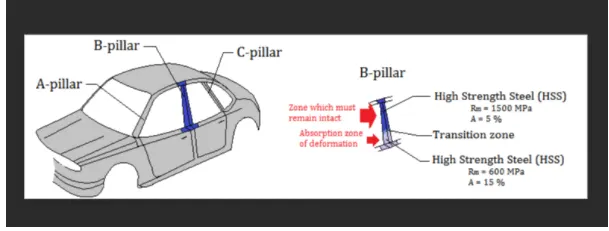
ABSTRACT :
The report details the Design Life Cycle in the Automotive Industry with an practical working model of B PILLAR COVER on the B PILLAR of Car Interior. The report explains the steps followed in creating the tooling axis followed by detailed methods in creating B-Surface, Class C Surface and closed body. The Attachment features creation is also reported by following the design guidelines and final analysis of Draft to prevent the failure and improve the feasibility of manufacturing the part in plastic injection molding.
DESCRIPTION :
MASTER SECTION
Master Sections are the guides for design requirements which shapes the component after technical styling of Class A Surfaces.The body frame is mainly composed of floor longitudinal beams, upper side beams, door sill beams, and front cover, the rear beam, A-pillar, B-pillar, C-pillar and other load-bearing beam structures are composed.
Master Sections are parameterized model of the vehicle body that outlines the guide for NPD Team
In this Report B Pillar Cover Creation with detailed procedures of Surface Development and Attachment features are covered
OVERVIEW DESIGN LIFE CYCLE AUTOMOTIVE INDUSTRY
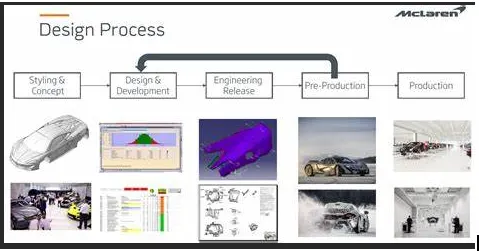
The Stages of Design Life Cycle are
Concept Sketches:
Concept sketches are rough ideas of free hand sketches obtained through a styling team and will be used to prepare the Model. It is usually done through pen and paper and through the painting software. This will be used to generate the concept for preparing the model by incorporating various styles and information obtained through the stakeholders.
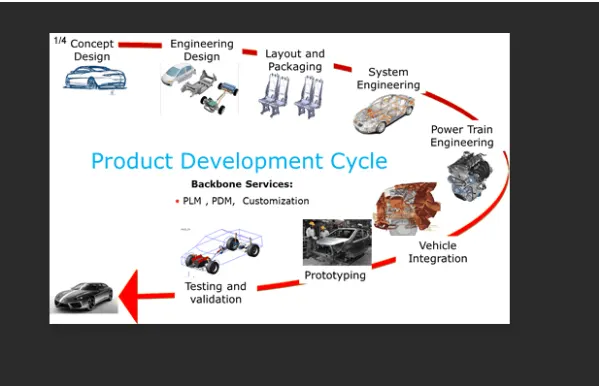
CLASS A Creation:
After finalizing the concept the sketches are usually worked in software such as Autodesk ,Alias to create Class A Surface
Clay Modeling :
The Class A Surface is concurrently worked by clay modelers to brainstorm and benchmark the styling of the product and later the Concept is validated by bringing up a rough clay model and then it is passed on to the Design team for the preparation of New Product Design (NPD) CAD.
C Surface Creation
Closed Body Creation
Draft Analysis
TOOLING AXIS
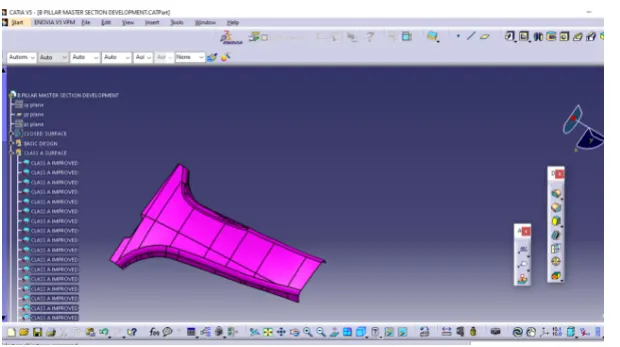
The given Class A input is analyzed to envision the part to manufacture and Tooling axis or Tooling Direction or Die line is the direction that molds pull apart in injection molding. There are two mold pieces named core and cavity. Thus tooling direction determines Mold separation and also becomes vital in developing the plastic product which is drafted to desired nominal angle for feasible clearance and ejection of final part from the mold.
The Steps Followed in creating Tooling Axis
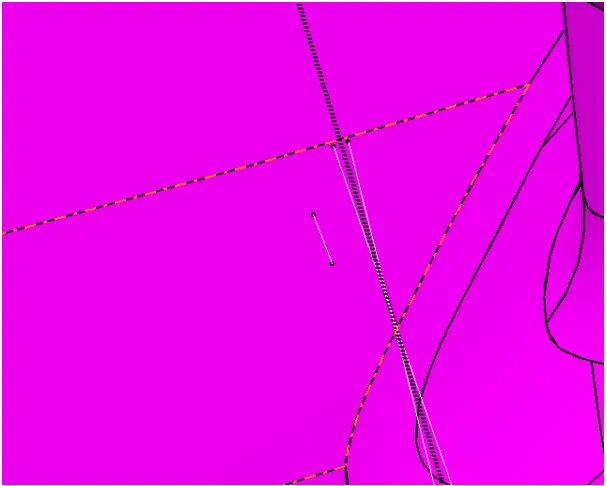
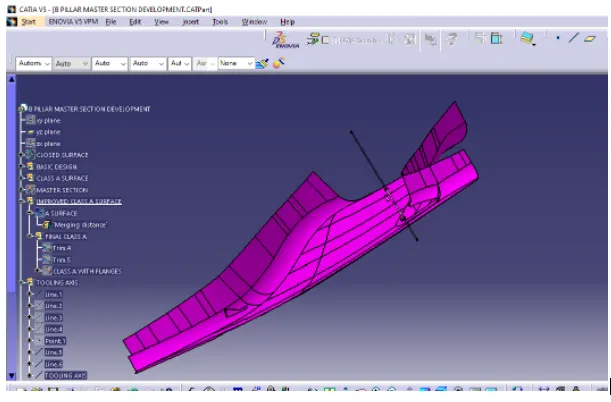
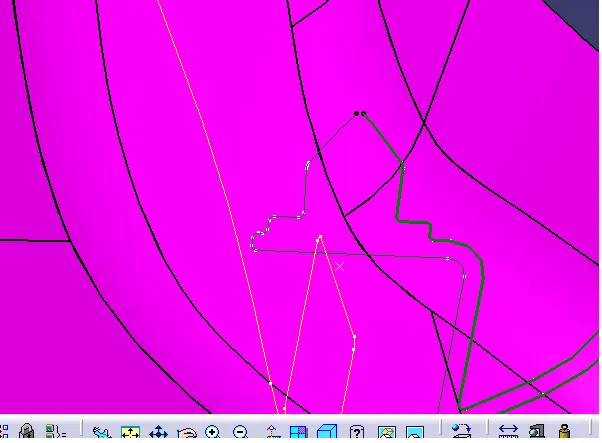
A Reference Point is created along the Surface zero and new Axis system is created
The X Direction and Y direction along the Class A were used to create Tooling direction
Finally the Tooling axis is created by bisecting the two lines and it is published. Class A Surface as input using surface operation commands Class B is developed
The tooling Axis determines the direction of Class C boundary swept with draft direction.
When viewing from tooling direction normal all the parts that are drafted should be visible so it gives an rough idea to determine product manufacturing in Injection molding
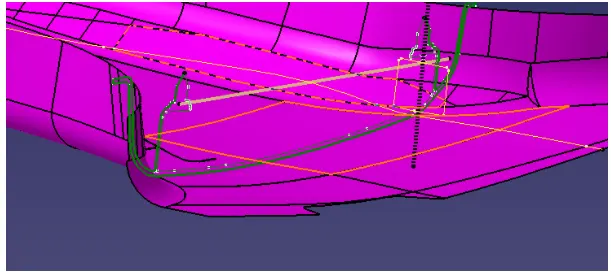
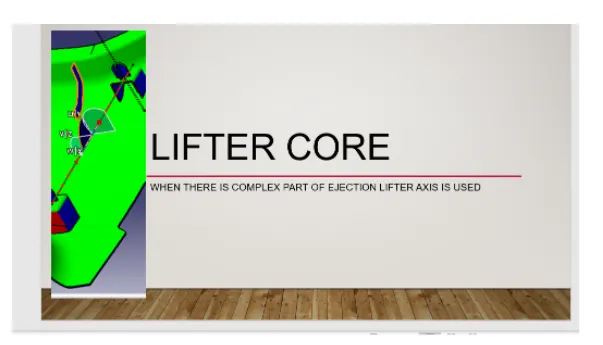
In B Pillar Model there are Two Tooling Directions one on Main tooling and other on Lifter Side that is used to eject the parts during injection molding
Lifter Axis is used because the Attachment feature is bounded by close walls
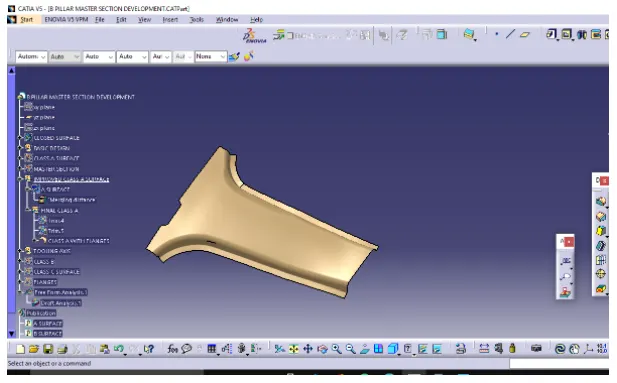
CLASS A IMPROVEMENT
Class A Surface is the outer skin of the product which is purely an aesthetic model with no engineering properties involved
The CLASS A Surface has lot of irregular patches and complexity which are improved using Multi Section Surfaces and Surface Trims which forms the Improved Class A Input
A Tangential Error Propagation method is used to validate the Surfaces using Boundary option.
The Class A has Flanges which are obtained through Master Sections and developed and Compared
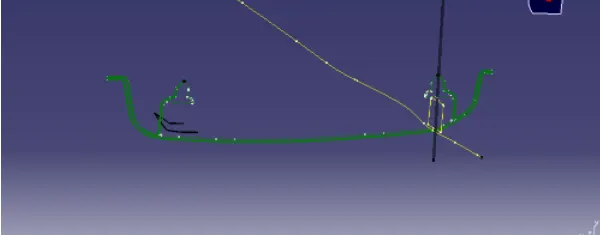
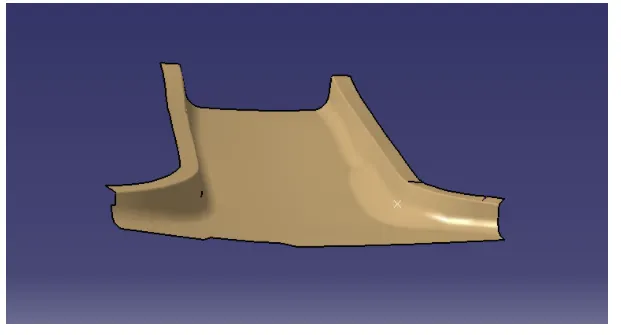
Finally the Class A Improved is used as input Model and is Published
B Surface creation
The next step is to design B surface for the input which is usually the surface where all engineering aspects and support creations are done.
The B surface Creation is performed using surface operations in CATIA which is an offset from Class A with dimension proportional to the thickness of the part
In B Pillar Design the B surface is offset 2mm from the input which is the thickness of the part
The B surface is an extrapolated surface compared to A surface and forms the bottom skin of the part
The Offset Surface leads to Surface Degenerations if
Rapid change in curvature or surface continuity
Low Radius of CLASS A
Conic or Styling Fillets
The Remedy is to untrim , extrapolate and trim or create surfaces using Multi Surface Option and Join
Corrected B Surfaces
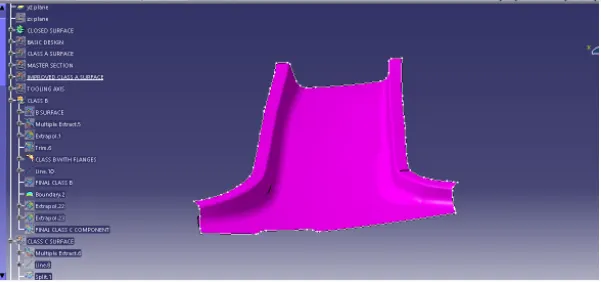
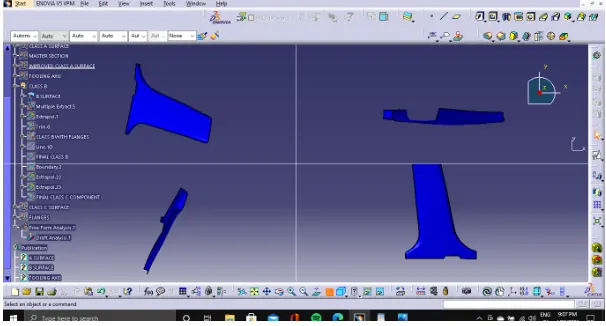
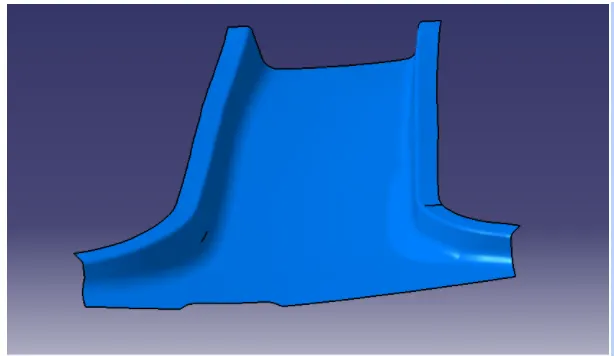
In this way the Patches are corrected along the B Surfaces and the part is Extrapolated with offset of 2mm from A Surface
C Surface Creation
The Next step is to from the C surface which is an intermediate surface between A and B and is used to give the closed surface appearance to the design
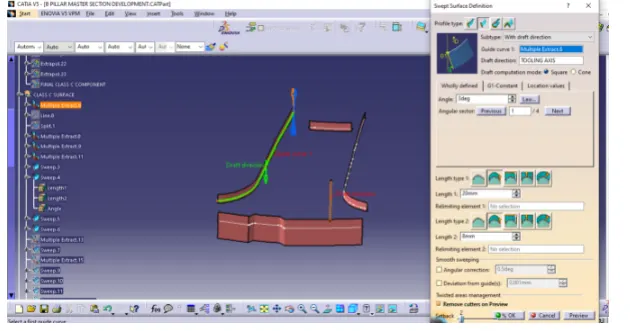
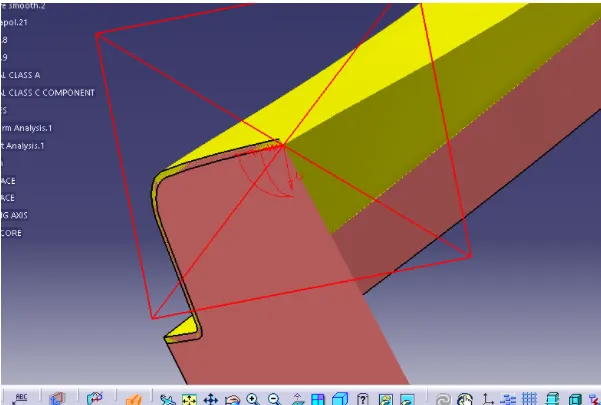
The C Surface is swept using the profile as the boundary line of Class A which is the Guide curve with a subtype along draft direction.
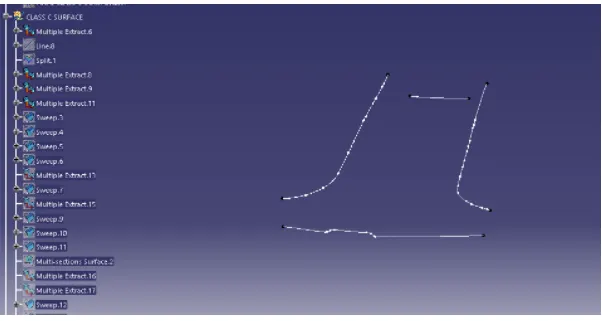
The Direction of the sweep is the tooling direction formed earlier
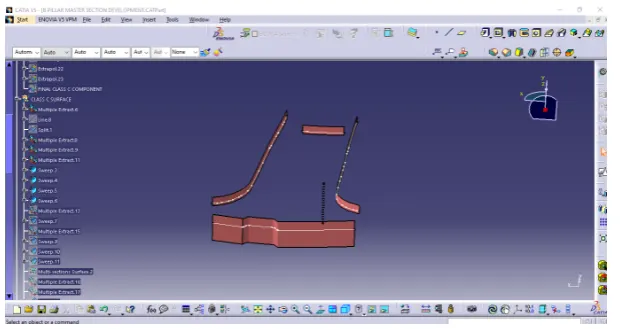
The draft angle for the sweep operation is provided which is 3 Degree and surface is swept for length above the thickness of the specified part
The C Surfaces must be drafted outwards from the A Side to avoid the parting Line along the A Surface
The C surface is refined using smooth Curve options to remove the complexity and patches along the swept surface
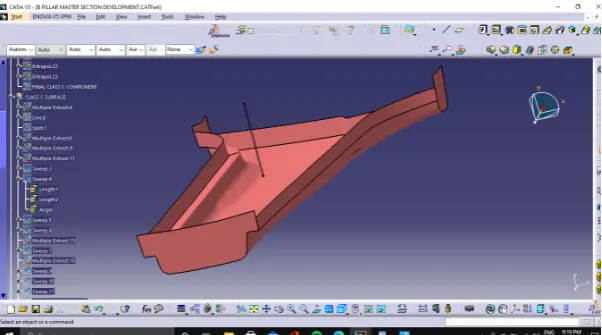
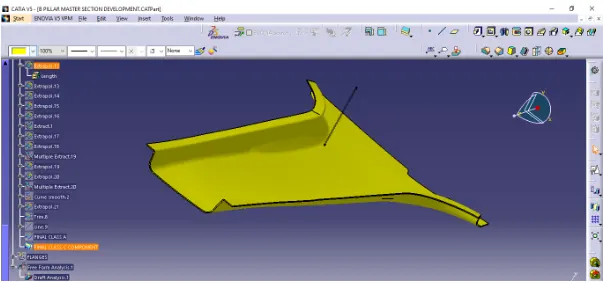
Finally the Class A and Class C surfaces are joined together and the connectivity of surfaces should be less than 0.003mm and the surfaces are merged.
C Surface merged with Class A
Closed Body Creation :
The merged surface is then trimmed with B surface to form the closed surface.
The Closed surface is then validated to find the irregularities along the edges and imperfections along the edges were then corrected using operation like extrapolate and surface trim
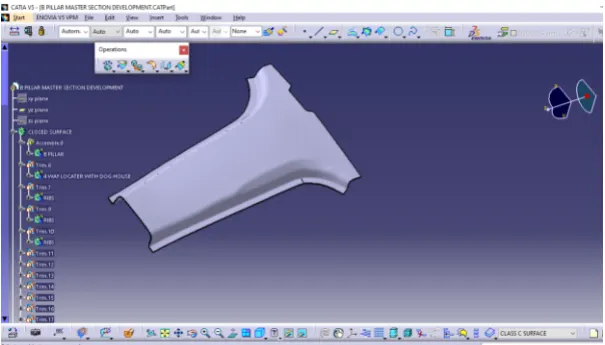
This Closed surface is the outer skin and finally the part is formed by Closed Surface in part design workbench
The final part is measured to validate the uniform thickness of the part especially along the filleted edges.
The Uniform Thickness ensures that the part Created does not form Sink Mark and Flow Lines along Class A
ATTACHMENT FEATURES
The Attachment features are the Fixation and Location features that Fixes the components The Common Attachment features used in B Pillar Are
Doghouse with 4 Way Locator
Ribs
DOGHOUSE
Using the Master Section the Doghouse is created and then part modelled using Thickness option
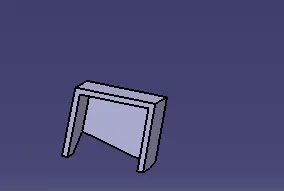
The 4 Way Locator is Formed above the Dog House which locates the B pillar towards the Mating Surfaces
The Dog House Design Rules are
The Thickness of the Connecting surface towards B Side should be 40% off the main thickness
The Walls are drafted with Min 0.5 Degrees along the Main Tooling Direction
The Attachment feature created needs a seperate tooling axis to clear the part Hence a Lifter Axis is used
The Surfaces that are cleared along the Lifter axis are also given a Minimal Draft
The Height of the attachment walls should be a minimum of 3 mm
This avoids the plastic defects on the B Side and maintains the texture of A Side
The Dog House with four Way Locator are shown below
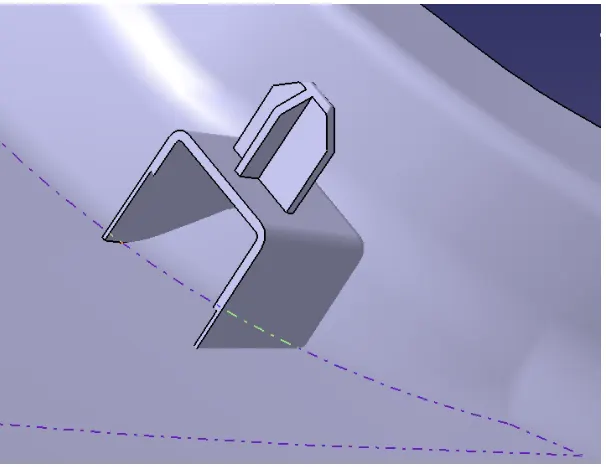
Four Way Locators are Tapered along the Edges to create an entry point for locators and the Locator Walls are drafted along the Main Tooling Direction.The Walls are minimum of above 0.4 times of the total Thickness to avoid shot incapacity during plastic product creations and the apex walls are ensured to be enough for creation of parts.
RIBS
Ribs provide stiffness to the parts and can be to impart toughness without increasing the part thickness and are locators and provide alignment to the mating parts
The Design Rules for two way and four way fixtures are
Rib Wall Thickness should be 0.4 times of Thickness of the part
The Drafted walls of rib should be within 0.5 degrees
The top height of rib should be at least 0.70 mm thick to allow the molten plastic to reach the top to avoid Short Shot
The Thickness of the Rib, Fillet Radius, Draft and rib root thickness are measured and are within the design specifications
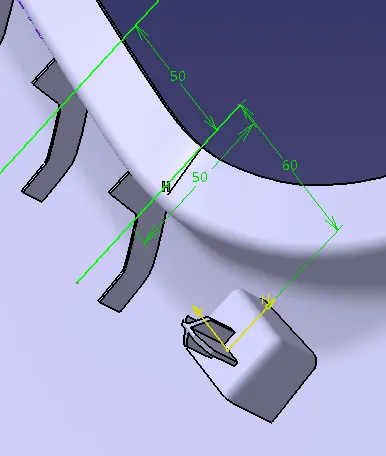
In B Pillar The Ribs are 50mm apart on both Sides
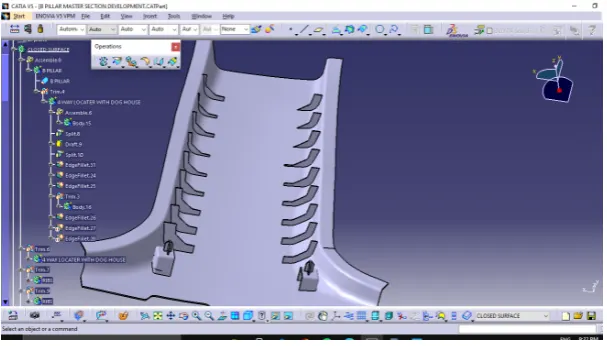
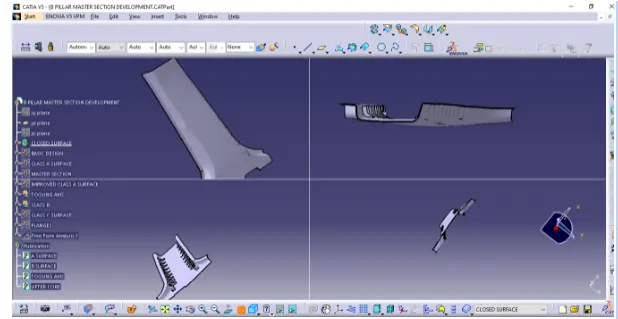
Thus B Pillar Cover is Surface Development is completed and attachment features are added.
It should be noted that the fixation of bolt locators always follows the 3-2-1 Taylor Principle.
Translational Movements along X,Y,Z Axis ( Positive and Negative)
Rotational Movement along X,Y,Z Axis ( Clockwise and Anticlockwise)
The Improvement in Given B Pillar could be an addition of another Dog House at an extreme end to satisfy the Taylor's principle and Thermal Stakes are provide that arrests all degrees of freedom and completely fits the B Pillar Part
DRAFT ANALYSIS
The finished part is then analyzed to detect if the drafted part will be easily removed from the injection molding.Draft Analysis option in CATIA is enabled through Insert> Analysis> Feature Draft Analysis
The Draft Analysis Icon has
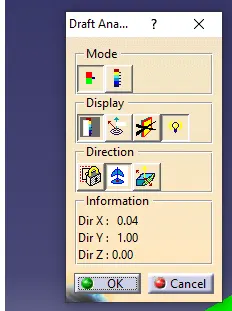
Mode
Display
Direction
Mode:
This is the color code that specifies the color to part based on the draft angles and is two types
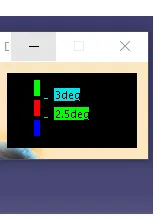
Quick Analysis
Full Analysis
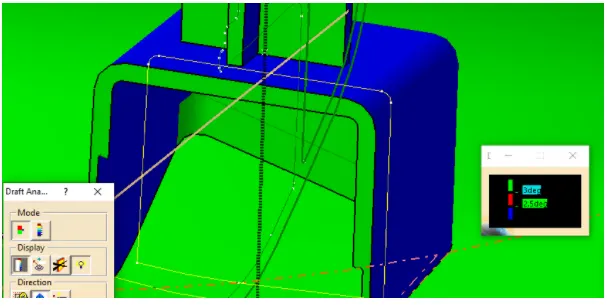
The Color code specifications for B Pillar DRAFT ANALYSIS
Display:
The various display modes are
Show/hide Color scale
Running point Analysis
Highlight Representations
Light Effect
The display options is used to refine the analysis and results
DIRECTION:
This is one of the important tool which
Compass Definition: This is used to pan the compass to the die line or tool direction.
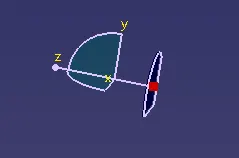
Lock Direction: This option locks the compass at the specified position
Invert Draft Analysis: which is used to invert the axis system and used to analyze the negative tooling direction
Draft Analysis Procedure
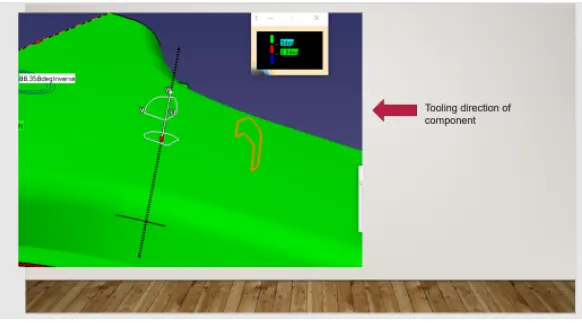
The part created has to be changed to material mode in display frame
Then by enabling compass definition the axis system is pan along the direction of the part and aligned in line with the tooling direction
Lock Direction is applied that fixes the compass and then the mode dialog box is formed by snapping at any point on the part
The Color Codes are classified and Draft Angle are applied
Then the Running point analysis is used to hover around the part to analyze the permissible draft angles and the analysis is saved
The Analysis is provided below
DRAFT REPORT
The Draft Report for B Pillar Model is shown Below
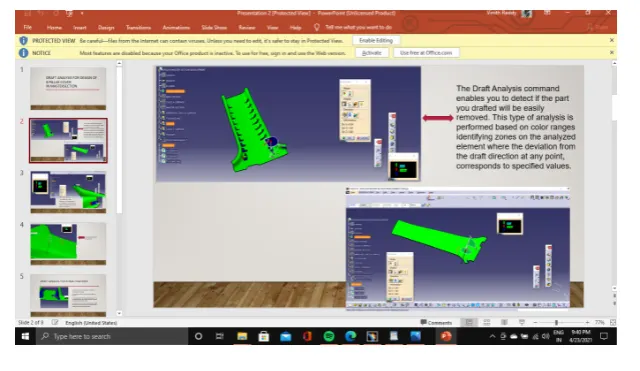
The Minimum Draft for All A Side Surfaces are 3 Degrees
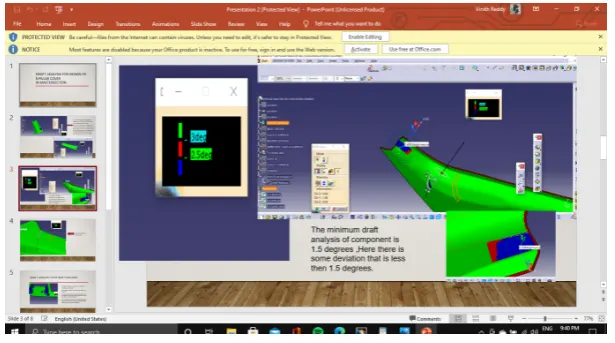
The Surfaces that are below 3 Degree are shown Below
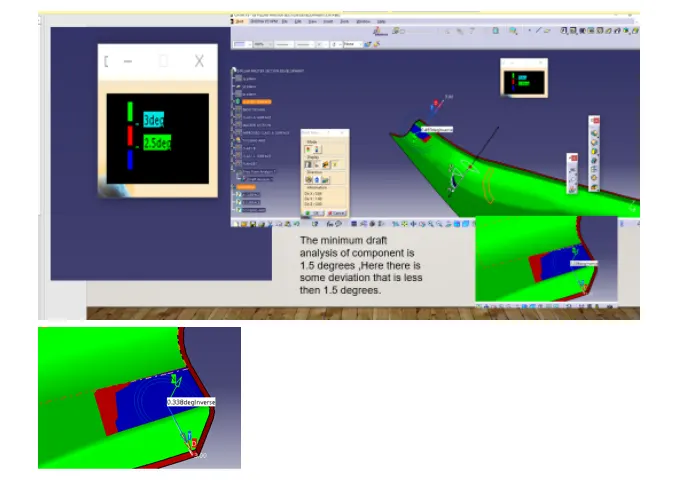
The B Side Surface Analysis is Shown Below
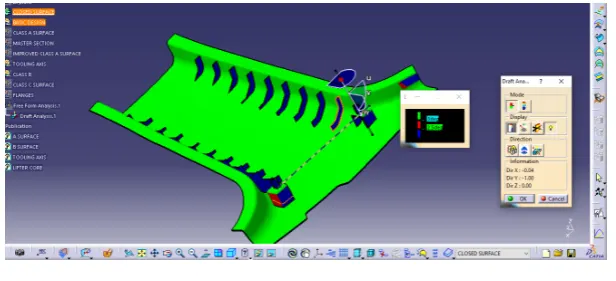
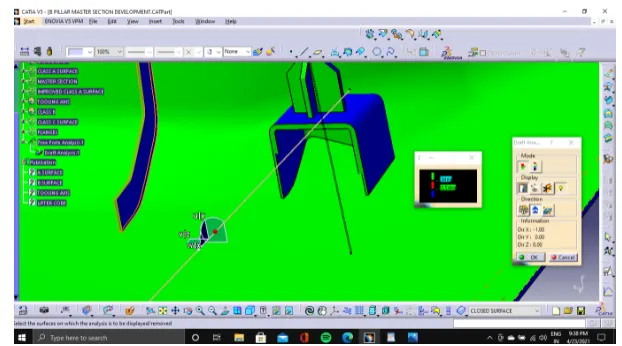
All The C Side Surfaces are are drafted and are below 2.9 degree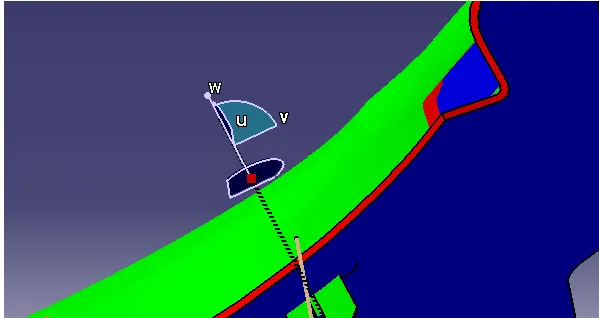
The Main Tooling Draft Analysis of the Attachment features are shown below
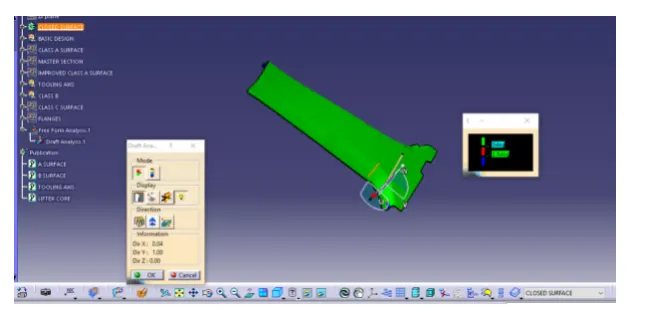
The Lifter Axis Draft Analysis are shown below
RESULT
The Green color is drafted walls above 3 degree
The Blue color is drafted walls from 0-3 degree
The red surfaces are negative degree
The analysis shows the drafted walls are above the par of 3 degree which is permissible to manufacture in the injection modeling
The Running point analysis hovered along the drafted walls show parts are above 3 and will be easily cleared from ejection.
The Areas in Negative Tooling that falls short to the permissible design Rules are shown
These surface are corrected using Surface Operations and generally in OEM Class A Improvement requires prior approval from Styling team and the draft report and analysis is used to get approval
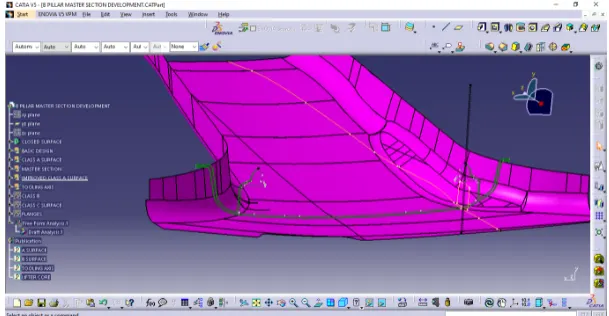
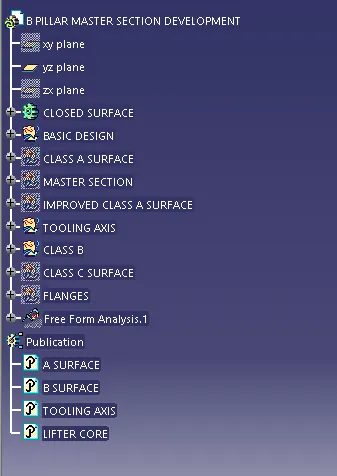
The Tree Structures are Classified and the important features are published and the operations are renamed and classified into geometric subset shown below.
Publication leads to easy access of parts rather navigate through the specification tree
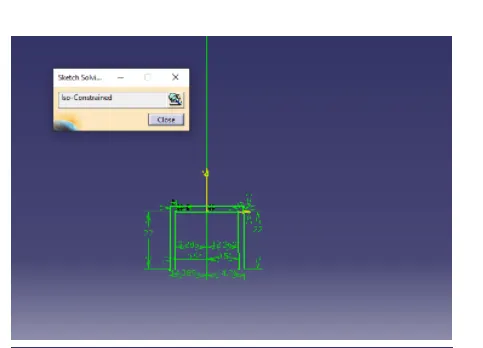
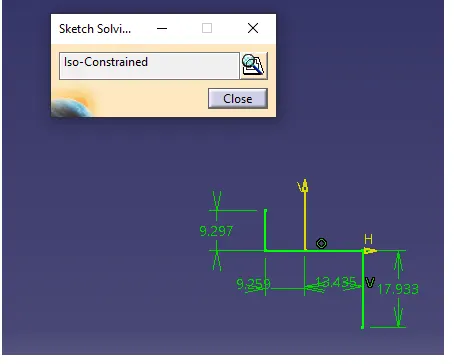
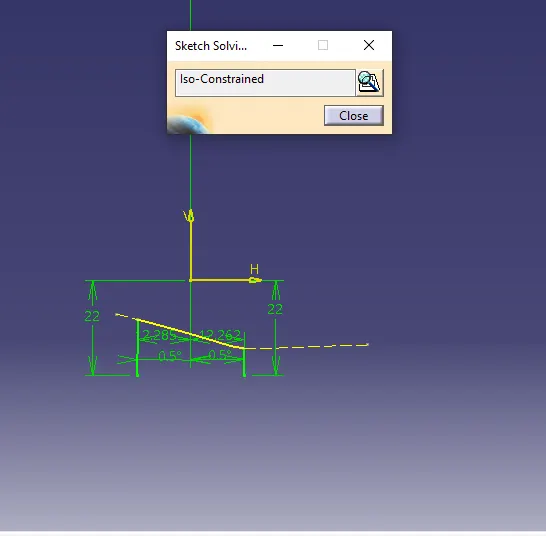
The 2D Sketch created for this operation are positioned sketches projected through a point and all geometries are fully constrained
CONCLUSION
Thus a Tooling Axis is created and an open aesthetic Class A Surface is developed into a closed surface with all plastic design rules and a final part body is created out of it in CATIA Surface WorkBench. The Design is then validated with Master Section and understood the use of Master Section Development in Product Design through development of B Pillar Cover used in the Car Interiors.
PLATFORM USED CATIA-v5
REFERENCE BY
https://skill-lync.com/forums/groups/skill-lync-plastic-design-for-automotive-applications-using-catia-v5