Week 9 - Project 1 - Door Trim Lower with Engineering Features
AIM:
- To create the Door Trim Lower Plastic component through the given Class-A surface. To begin with, the tooling axis for the given Class-A Surface should be created meeting the requirements of the draft angle and at the end perform the Draft analysis on the model.
- To create the Heat Stakes and the locators considering the design rules
Objective:
First, you will need to generate the requisite proper Tooling axis, and then you will execute the Draft analysis on the class A surface that has been provided. By utilising the surface modelling tools, you may create the class-B surface as well as the class-C surface. Additionally, the closed surfaces of classes A, B, and C should be combined into a single solid body. In addition to this, carry out the Draft analysis on the solid model.
The Tooling Axis is as follows:
In injection moulding, the Class-A surface is initially evaluated to determine the tooling axis, also known as the tooling direction, along which moulds pull apart. Tooling direction is critical for the design of plastic products because it determines the path that mould separation will take.
Draft Analysis:
For moulded or cast pieces, the degree of taper that runs perpendicular to the parting line is referred to as the Draft angle. The temperature can be expressed in degrees. In order to decrease the possibility of the parts being damaged and to guarantee their ejection, a functional part for injection moulding needs to have draughts facing both the cavity and the core sides. In order for the part to detach from its housing in the correct manner, it is essential to beat the vacuum forces by allowing air to enter the space between the metal and the plastic. incorporating while keeping a respectable cosmetic appearance. For both the production and the plastic product, there should be a draught included in the design. At the very beginning of the design process, the designer ought to be aware of its necessity. Because of this, design requirement factors can be taken into account.
Creation of the tooling axis:
The following is the technique for tooling axis:
- In order to manufacture a plastic item using injection moulding, a Core, a Cavity, and Sliders are required.
- The Core, the Cavity, and the Slider all move and sideways in a specific direction that is referred to as the Tooling Axis.
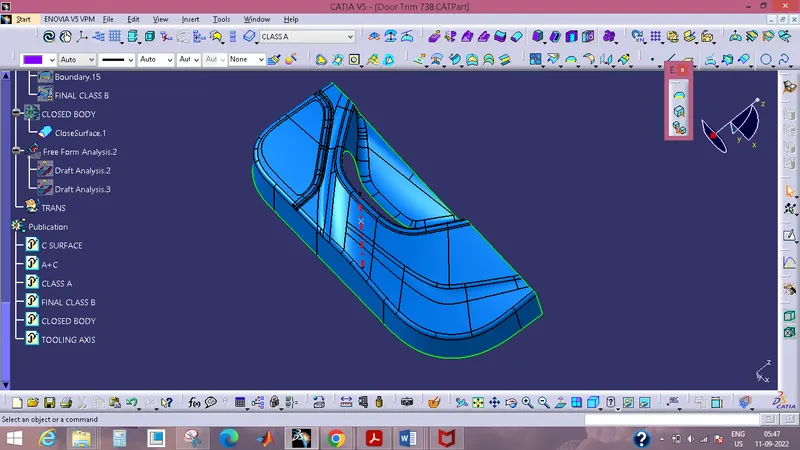
In most cases, the tooling axis is conceived of by employing the method of bisecting a line or plane. On the other hand, the tooling axis is assumed to be a line that is normal to the base surface of the bin in those components where it is present. The same approach is taken with regard to this component. Drawing a line that is parallel to the base surface will result in the creation of a tooling axis. The number of offelemts that are allowed should be as low as possible.
In order to determine whether or not a component may be manufactured along the tooling axis, a drafts analysis is run on the class A material. During the process of doing a draught analysis, it was discovered that the bin walls make an angle of ninety degrees with the foundation. There is not a predetermined minimum draft that the walls must adhere to. We are not permitted to make any modifications to the class A surface; however, we are able to notify the class A designer that the walls should have a minimum drafting.
Draft analysis of Class A:
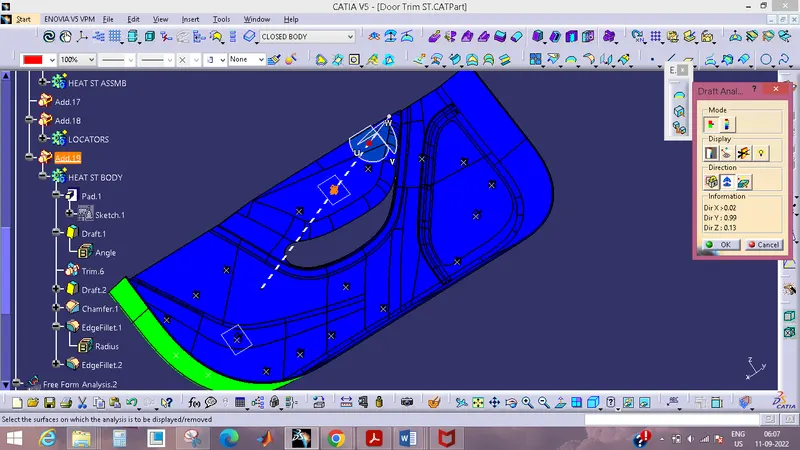
After defining an axis for the instrument, we go on to the drafting analysis. Before we can begin the drafting process, we need to make certain that the materials are selected in the view mode.
After selecting the feature drafting analysis tool, we move the compass from where it was to where the tool axis is located by dragging it. The compass must then be locked. After that, select any part of the component, and it will provide the result to you.
We adjust the component's minimum drafting requirement to three degrees.
Checking the component's angle can be accomplished through the usage of the running point option.
We even have the ability to change the hue to better suit our tastes.
CLASS B SURFACE CREATION:
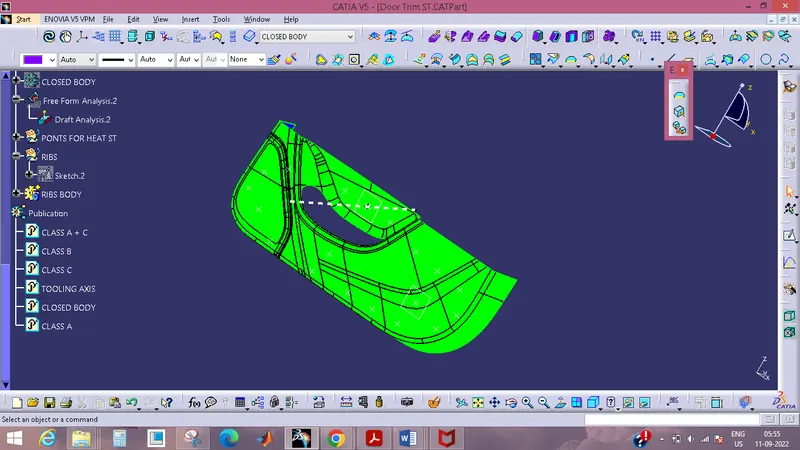
Using the Extract Command, a collection of surfaces were extracted from the Class A surface in order to produce the Class B surface. This is demonstrated in the image below.
It is possible for us to produce a Class B surface by first using the extract command for all of the surfaces that are necessary, and then using the untrim command to restore the surface up to the limit.
Class B Surface refers to the surface at which features such as side walls, base walls, top walls, outer walls, and other such elements are made to accommodate external mountings.
To create a Class B Surface, one must first extract an A Surface, then offset it to the necessary thickness, and finally trim the two surfaces together.
Considering that this is a complex component, we first establish the class B surface, and then we separate some surfaces in accordance with that by assigning some colours to the surfaces for our convenience.
SURFACE OF CLASS C:
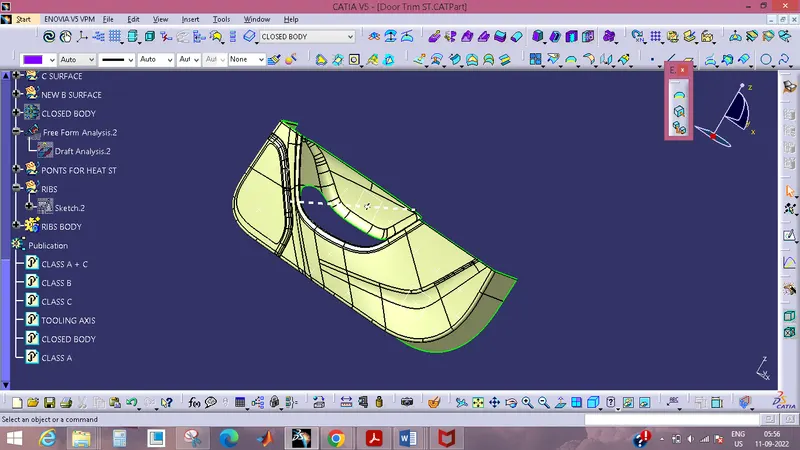
The Class C surface is an intermediate surface that connects the Class A surface and the Class B surface.
When making a Class C surface, the Draft angle and Tooling direction are both taken into consideration.
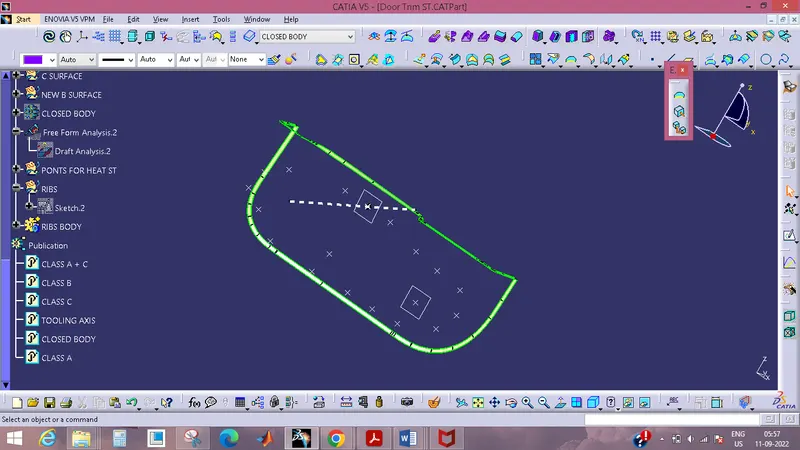
Now Join C & A Surface:
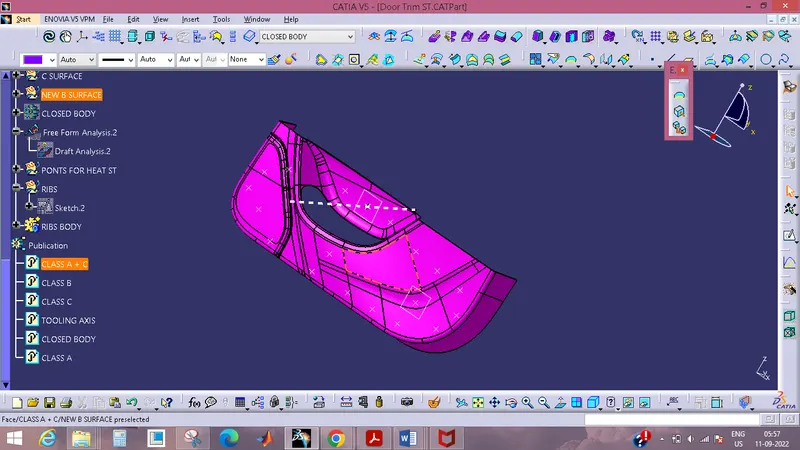
PART BODY:
After constructing a closed body, the next step is to construct a solid body by using the closed surface as a starting point. Proceed now to the part workbench in order to create the sloid body by utilising the closed surface command.
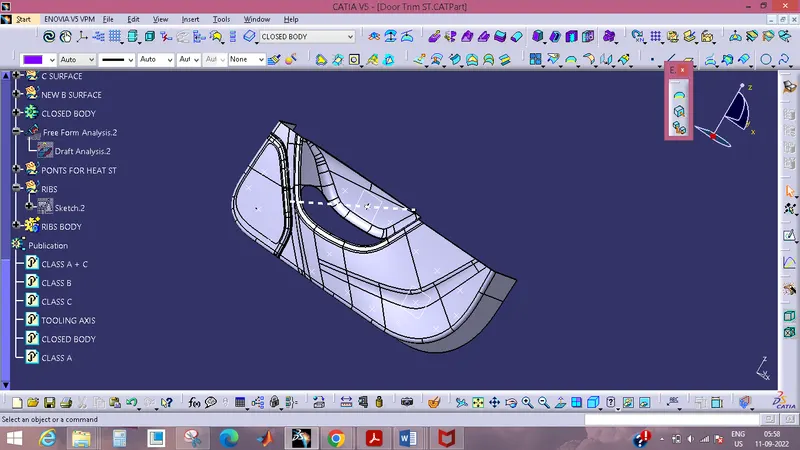
Create 4-way locators and heat stakes:
INTRODUCTION:
3-2-1 PRINCIPLE:
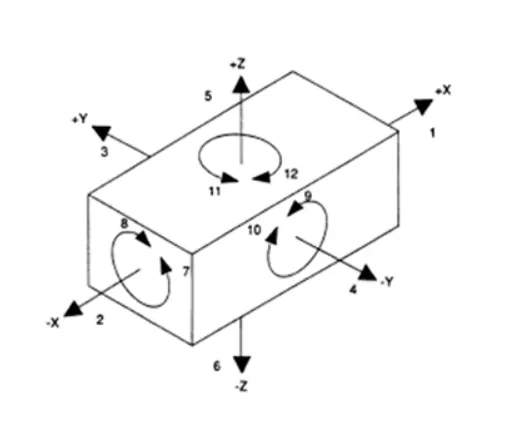
A piece of work that is floating freely in space is able to move in an unlimited number of different directions. This action can be split down into 12 constituent parts for the purpose of analysis.
movements in a certain direction, often known as "degrees of freedom." In order to guarantee accurate reference of a work item, each of the 12 degrees of freedom must be constrained.
As can be seen in Figure 1, each of the 12 degrees of freedom is connected to the work-central piece's axis in some way. Take note of the 6 degrees of freedom that are axial and the 6 degrees of freedom that are radial.
The axial degrees of freedom allow for movement in a straight line in any direction along the three primary axes, which are denoted by the letters X, Y, and Z. The rotating movement that is possible thanks to the radial degrees of freedom can go in either a clockwise or counterclockwise radial direction around the same three axes. Rigid bodies have a limited number of degrees of freedom.Take into consideration the immobile object pictured below, which is located in the void of space. It is possible for it to have 12 degrees of freedom.
4-WAY LOCATORS:
4-way means that you prevent movement on the plane along two of its axes (+X, -X, +Y, and -Y). In most cases, the pin on the fixture will be cylindrical, while the hole in the workpiece component will be circular.
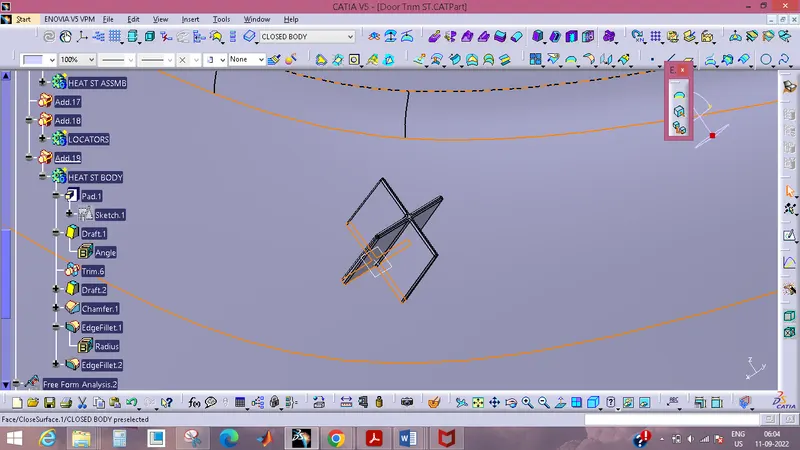
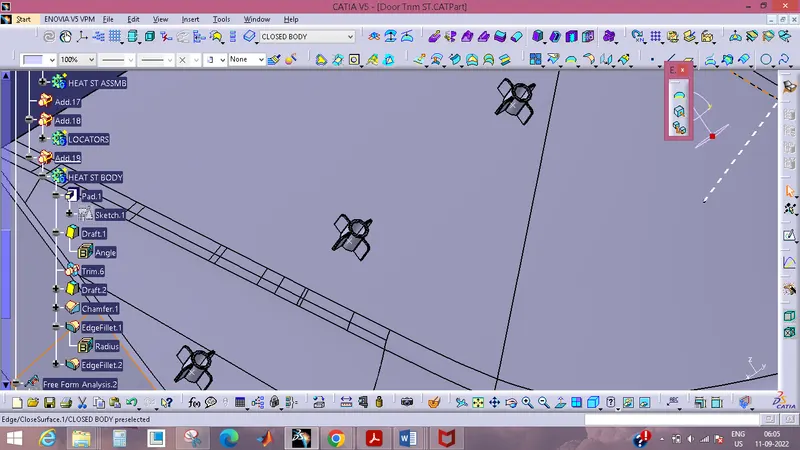
HEAT STAKES:
Currently, there are a wide variety of distinct combinations of attachment methods that are used in manufacturing operations to keep components together.
Permanent attachments can be created with common fasteners like bolts, screws, and rivets, but there are also attachment methods that don't use these common fasteners.
techniques that don't call for any additional pieces of gear. One of these techniques is called heat staking, and unlike the other methods, it does not require any additional fasteners.
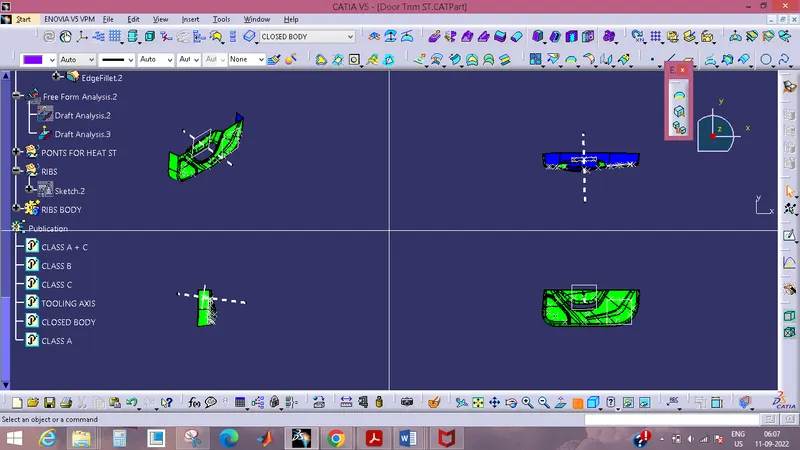
ALL VIEWS:
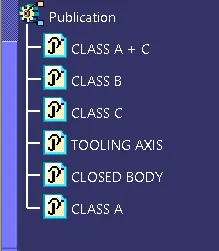
PUBLICATION
Publication of the component is done in order to make it visible and straightforward to navigate.
To publish the component, pick the tooling axis and the class A surface after going to the tools menu and selecting the publishing option.
Under the primary component of the tree, a separate tree structure is generated.