(ANSYS_P7)- Rolling operation
ROLLING OPERATIONS
In metalworking, rolling is a metal forming process in which metal stock is passed through one or more pairs of rolls to reduce the thickness, to make the thickness uniform, and/or to impart a desired mechanical property. The concept is similar to the rolling of dough. Rolling is classified according to the temperature of the metal rolled. If the temperature of the metal is above its recrystallization temperature, then the process is known as hot rolling. If the temperature of the metal is below its recrystallization temperature, the process is known as cold rolling. In terms of usage, hot rolling processes more tonnage than any other manufacturing process, and cold rolling processes the most tonnage out of all cold working processes. Roll stands holding pairs of rolls are grouped together into rolling mills that can quickly process metal, typically steel, into products such as structural steel (I-beams, angle stock, channel stock), bar stock, and rails. Most steel mills have rolling mill divisions that convert the semi-finished casting products into finished products.
There are many types of rolling processes, including ring rolling, roll bending, roll forming, profile rolling, and controlled rolling.Below is an image explaining the operation.
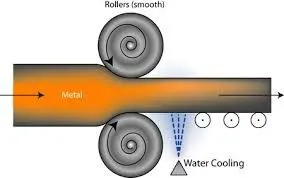
OBJECTIVE:
The aim of this simulation is to replicate this rolling operation using ANSYS workbench. Using copper non-linear material, this simulation is analysed by examining the structural integrity of the material after rolling.
TASK
For this challenge, I will have to simulate the rolling operation on a workpiece made of copper. The model workpiece length is increased by 60mm and decreased on both sides by 8mm. The simulation is run for 14 steps and you random values of displacement is defined to feed the workpiece into the roller. Ensuring that the edge of the workpiece is displaced by 90mm.
Find out the
- Equivalent stress for the whole setup
- Equivalent Plastic strain for the workpiece
- Directional Deformation in the Z axis for the workpiece
- Prove that the workpiece has displaced by 90mm
GEOMETRY
The geometry is imported into the workbench and edited using space-claim.
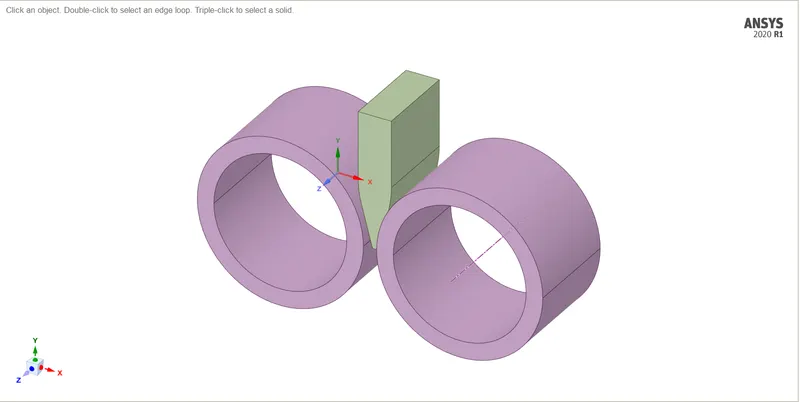
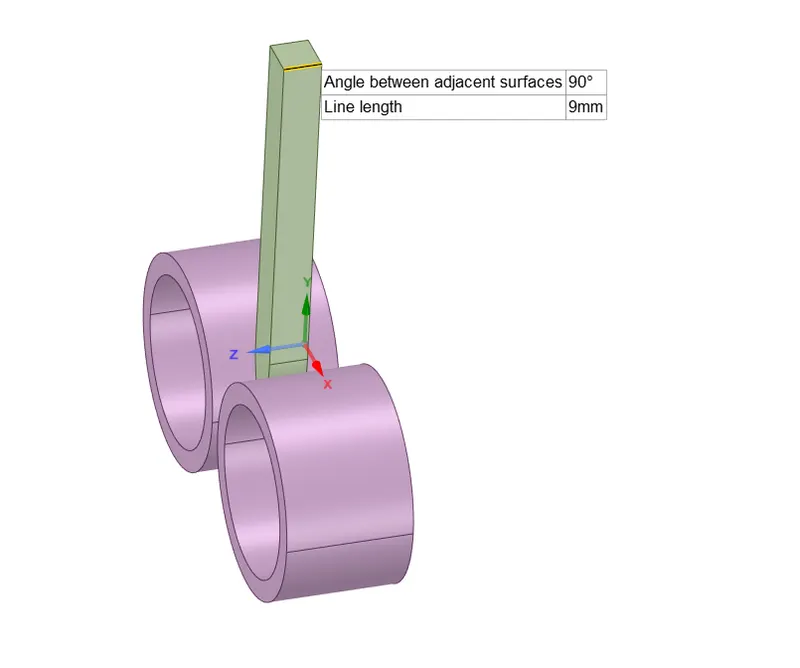
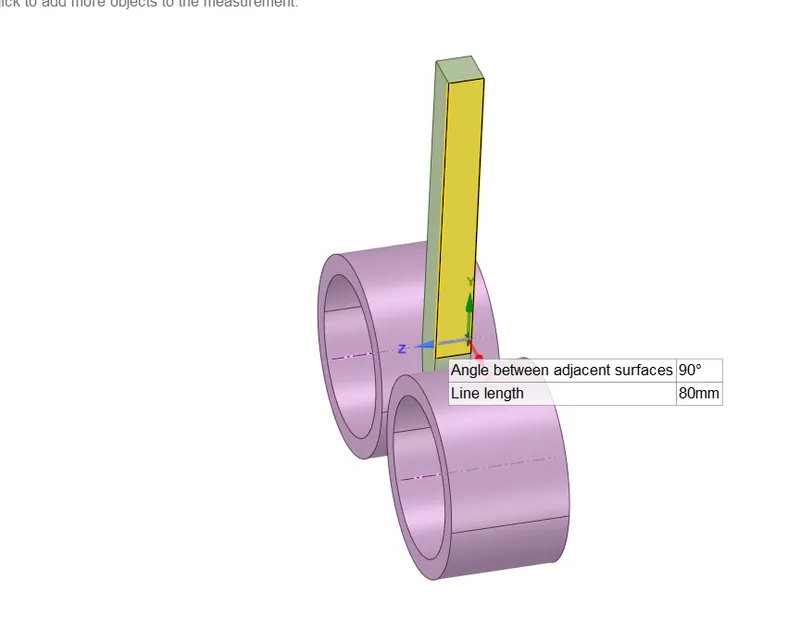
- In space-claim, the height of the model is increased by 60mm
- The width is reduced by 8mm on both sides
- Model is updated and mechanical bench is opened
- Edited model can be seen below
MATERIAL AND THEIR PROPERTIES
Stainless Steel-(Wheels)
Density: 7850 kg/m^3
Youngs Modulus: 200000Mpa
Poisson Ratio: 0.3
Tensile Yield Strength: 460 Mpa
Copper Non-Linear (Workpiece )
Density: 8300 kg
Youngs Modulus: 110,000 Mpa
Poisson Ratio: 0.34
Tensile Yield Strength: 280 Mpa
MESHING
Body Sizing: 4mm (workpiece)
Global Element Sizing: Default
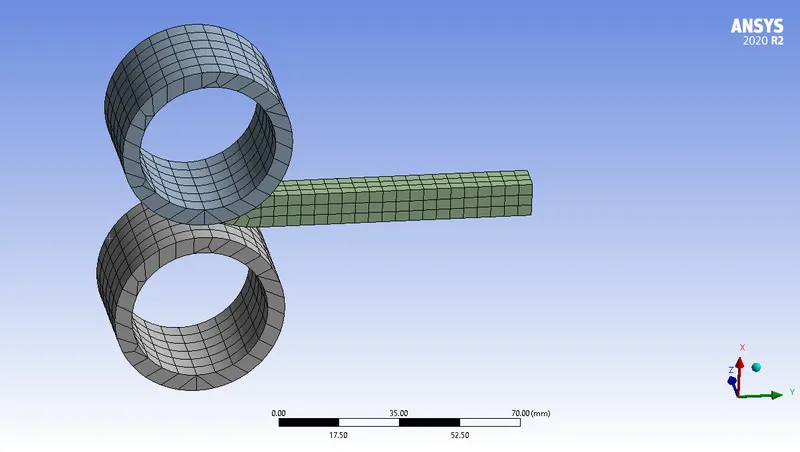
PROCEDURE
CONTACT
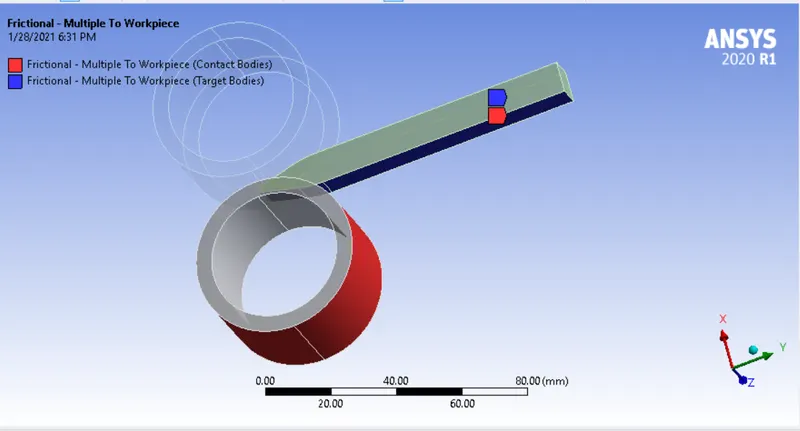
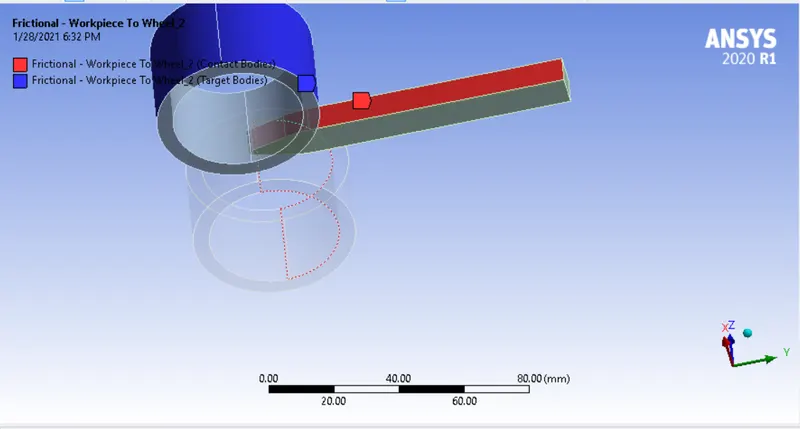
- The contacts between the wheels and the workpiece are specified with frictional type connection.
- The contacts are flipped to assign the wheel as the target and the workpiece as contact.
- Friction value of 0.2
- Augumental Langrange
- Normal Stiffness factor of 0.1
- Update stiffness by each iteration
- Interface treatment of add offset and ramped effect
BOUNDARY CONNECTIONS
JOINT
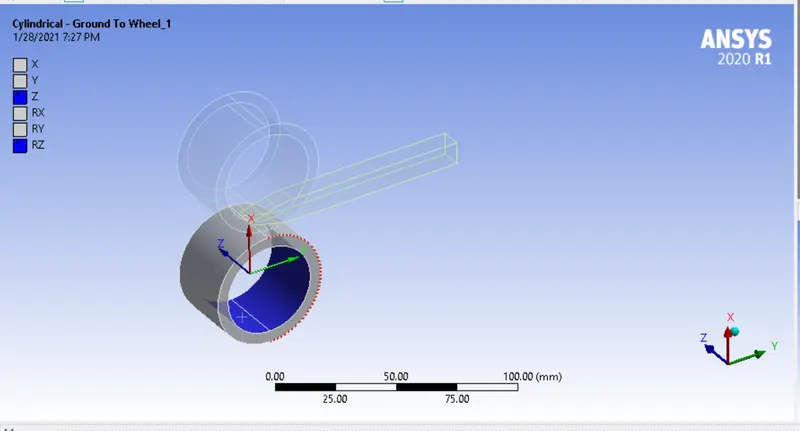
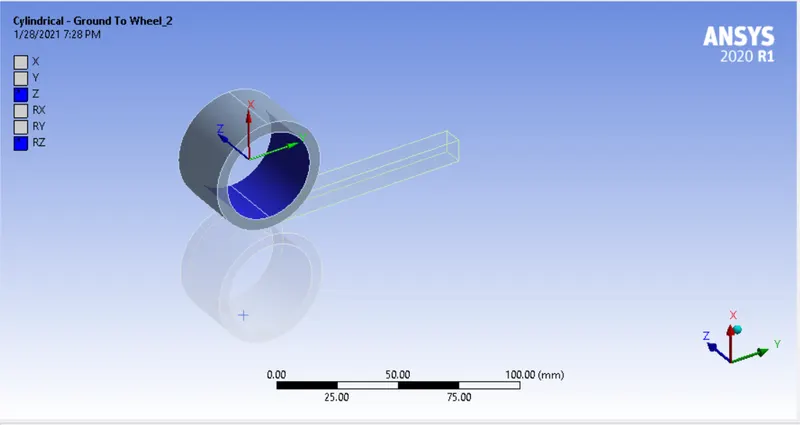
Two cylindrical joints are defined to the wheels with body to ground configuration.
JOINT LOAD
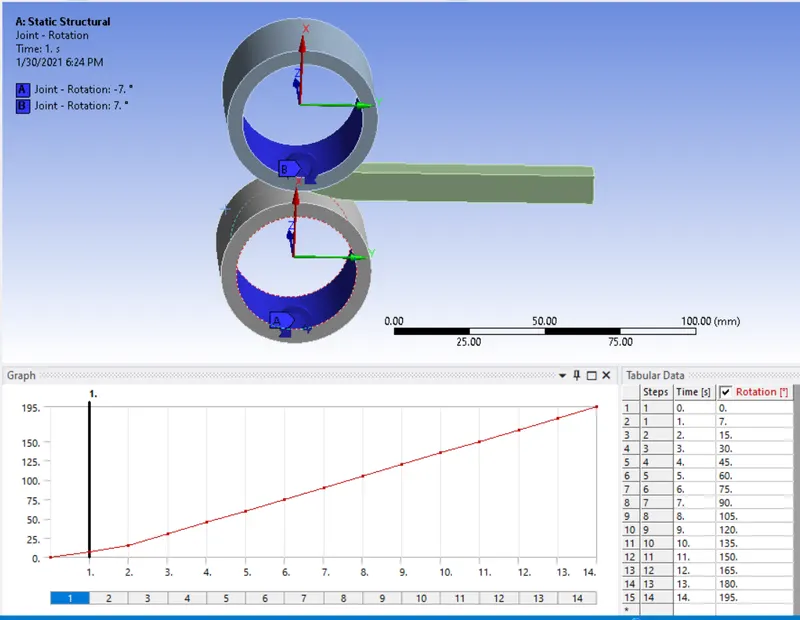
- Joint load is specified to define the rotation of the wheels about the Z-axis.
- Below is an image showing the rotations defined to control the wheel movements
DISPLACEMENT
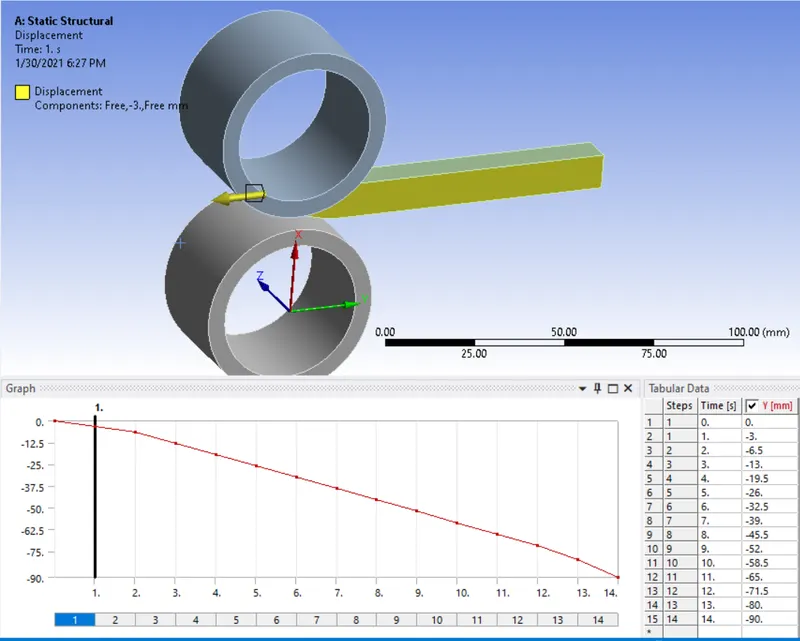
- Displacement of the workpiece in the negative Y-axis is definrd here
- The two side faces of the workpiece is selected and the displacement is defined sing tabulated Y-axis values which can be seen below.
- In order to ensure the workpiece displaces by 90mm , the last step is specified as 90mm displacement
ANALYSIS SETTINGS
Auto Time Stepping: Program Controlled
No of Steps : 14
Large Deflection : ON
Stabilization :Constant
Method : Energy
Energy Dissipation :0.1
Solver Type: Program Controlled
SOLUTION
Solution specified is.
- Equivalent stress for the whole setup
- Equivalent Plastic strain for the workpiece
- Directional Deformation in the Z axis for the workpiece
- Prove that the workpiece has displaced by 90mm
RESULTS
- Equivalent stress for the whole setup
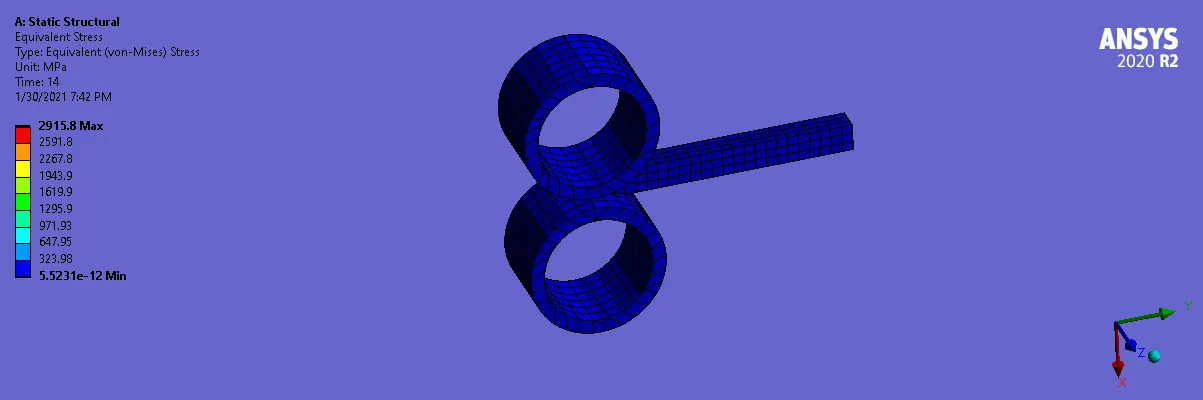
The maximum stress developed was found on the far end of the workpiece. As the workpiece id fed into the roller more resistance to deformation is formed at the endof the material workpiece. The maximum stress was seen to be 2559.9Mpa
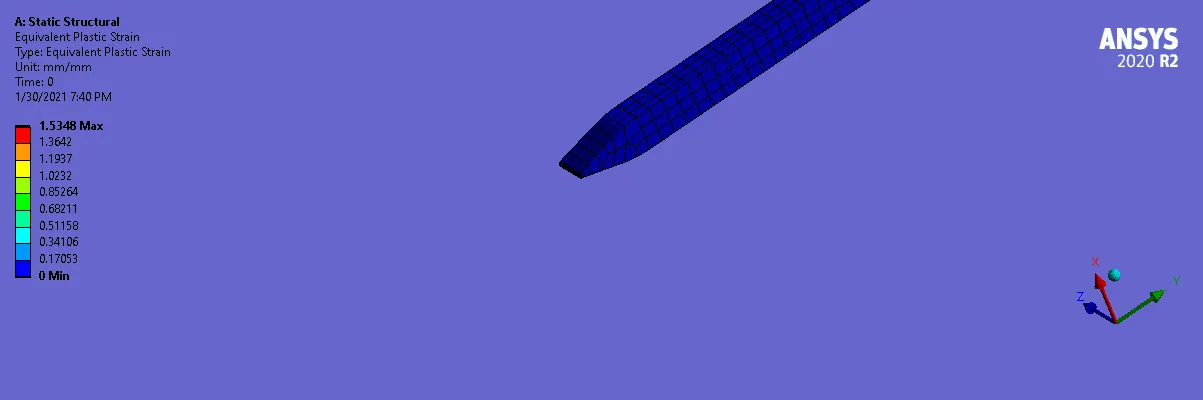
- Equivalent Plastic strain for the workpiece
Maximum platic strain : 1.5
- Directional Deformation in the Z axis for the workpiece
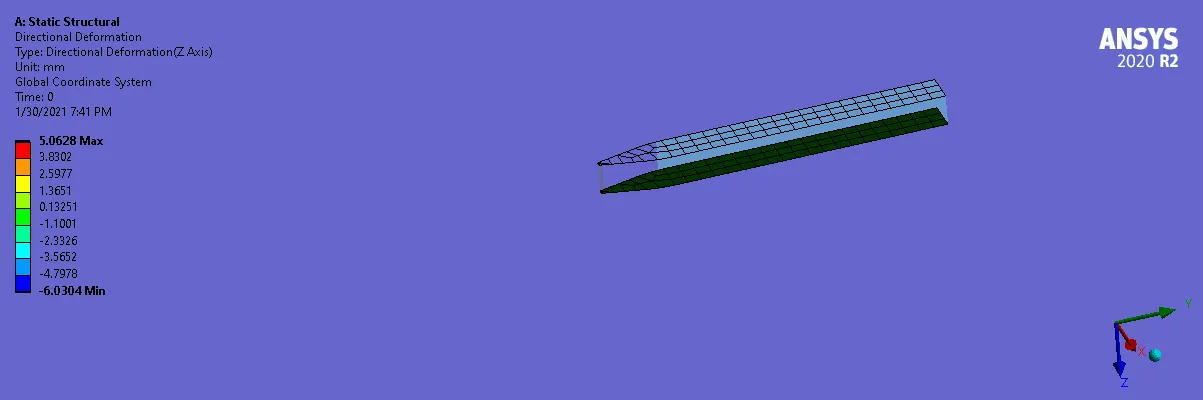
The directional deformation in the Z-axis was found to be 4.7mm
The draught which is the change in thicknes of the material is [10mm(initial) - 4.7mm(final)]
= 5.3mm
- Prove that the workpiece has displaced by 90mm
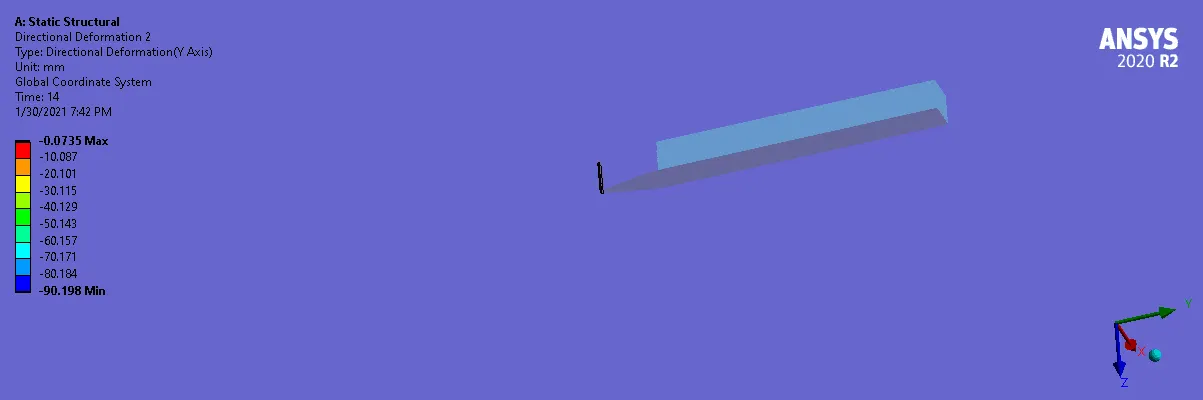
The results from the simulation below proves that the specified displacement was succesful and the workpiece was fed into the roller by a deformation of 90mm
CONCLUSION
A simple roller operation was demonstrated succesfully. This process is used by engineers to improve material per required specification.