Week 12- Final project
REPORT
DESIGN AND DOVELOPMENT OF DOOR INTERIOR TRIM
OBJECTIVE:
objective for this project is to make half of the door trim panel in catia-V5 from the provided Class-A surface of the same.
ABSTRACT:
This report contains a brief theory on design rules and the approach followed to achieve the final plastic product. Draft analysis report on all the class-A surface apart from the procedure to make the class-B and class-C surface is also mentioned.
APPROACH:
Our basic approach to make a plastic model from class-A surface should be:
- Run draft analysis
- Make tooling axis
- Make B surface
- Make C surface
- Trim all together and make it solid.
INTRODUCTION :-
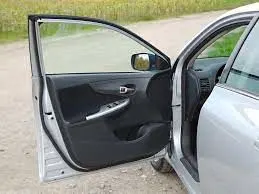
Ten stages in automotive product life cycle developement are listed below .
1)Concept sketch
2) Styling class A
3)Feasilbility check
4)Concept validation
5)New product design
6)Product developement
7) Prototyping
8)Design validation
9)Pilot production
10)Mass production
Designing Steps involved :
Given below is the procedure to create a new plastic component from given class A surface .
1) Creation of tooling axis
2) Creation of class b surface
3) Creation of class C surface
4) Creation of closed body
5) Draft Analysis .
CLASS-A SURFACE
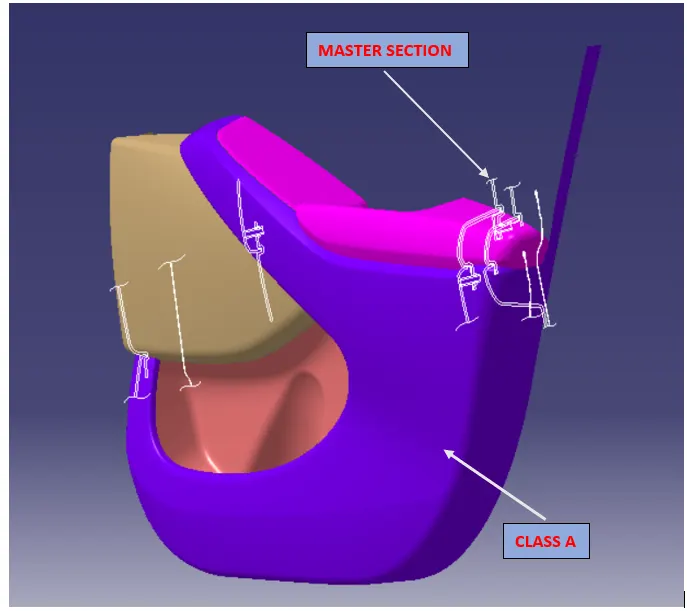
In automotive industry various teams works on various components, a car for example is not entirely designed by a single designer. There are many teams among which the task of making various components is distributed. And this is followed for every department of the industry. In this project we are given class-A surface which is designed in other software like Autodesk Alias, by a class-A designer. This is aesthetic surface and a lot of time, effort and good experience are demanded for making this continuous and a good flowing surface model. This is the major reason why, when we get this as input we are not allowed as a plastic designer to make any improvements in the class-A surface. Rather, it should be brought to the attention of the seniors which later is conveyed to the concerned team and take care of.
TOOLING AXIS
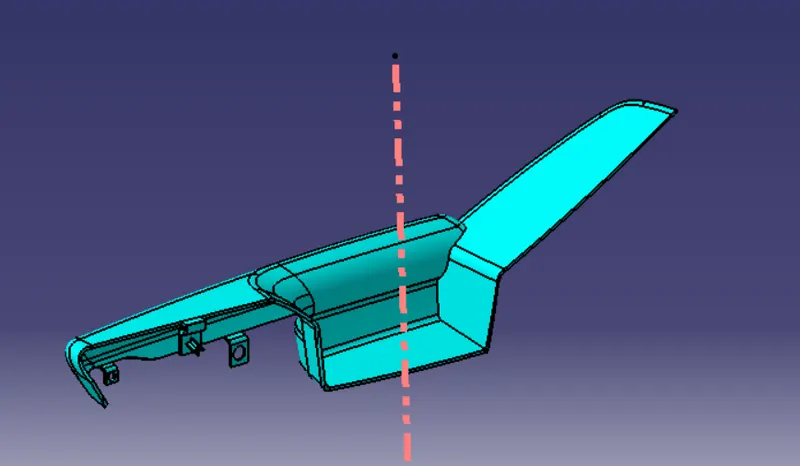
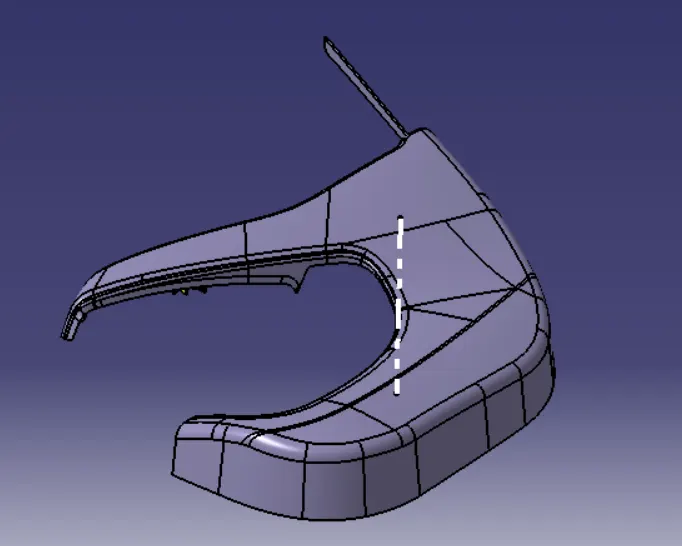
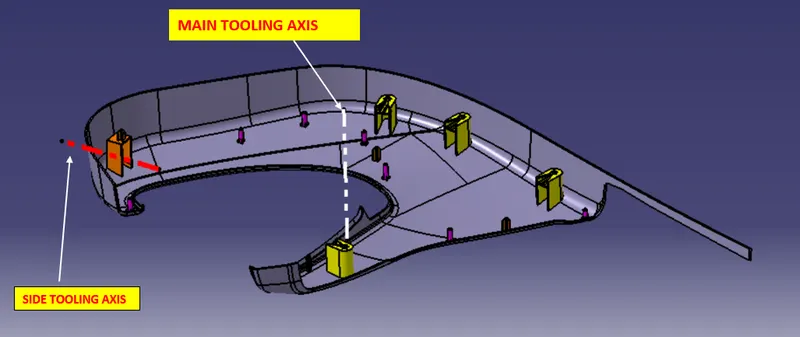
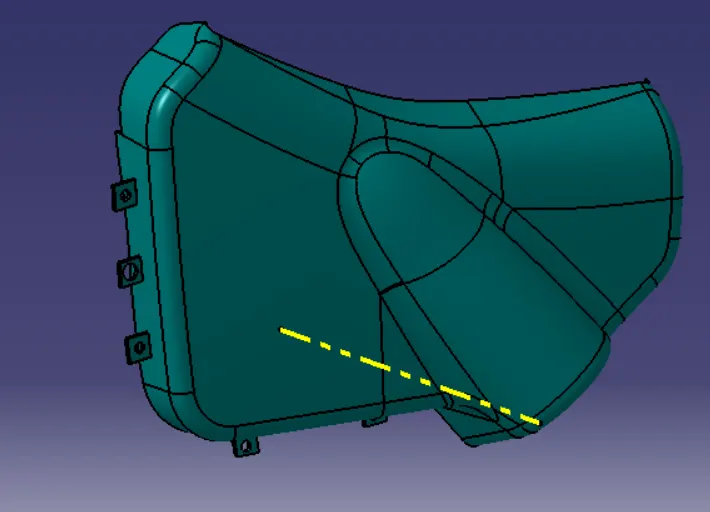
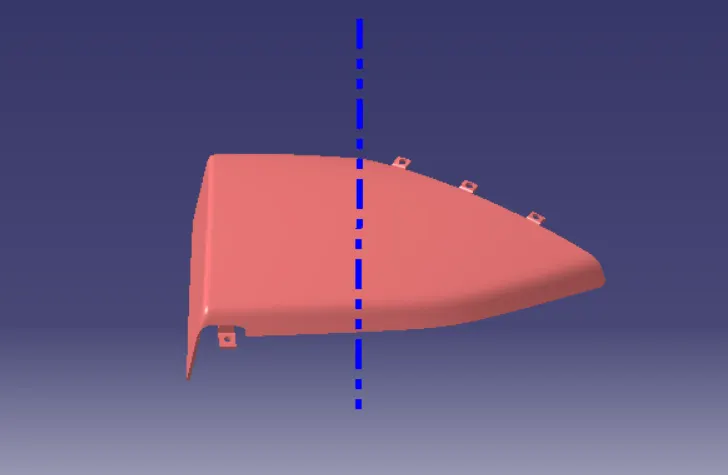
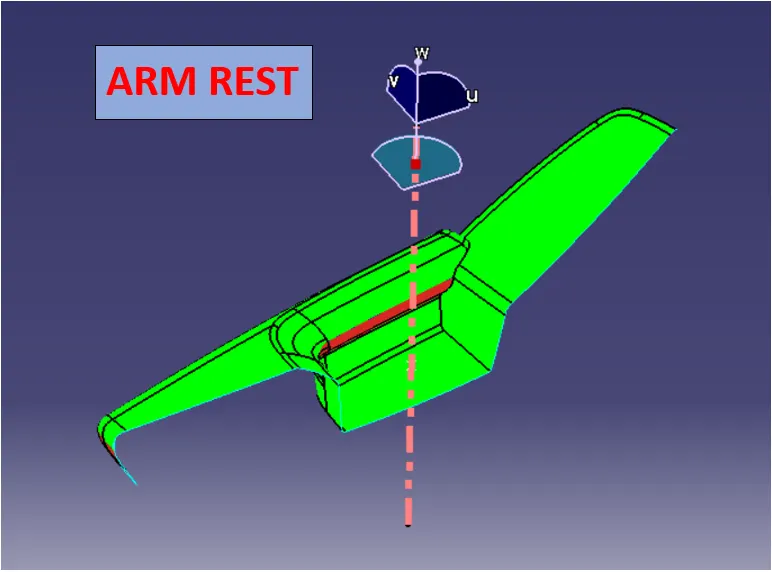
Tooling axis is the axis along which the core and cavity opens and closes. It is very important to define the tooling axis in the first step while designing a component as it is the main component which helps us to run draft analysis on class-A at initial stage to see if we can move ahead. Also for later stage, tooling axis is the direction along which class-C surface and the draft to the components is given.
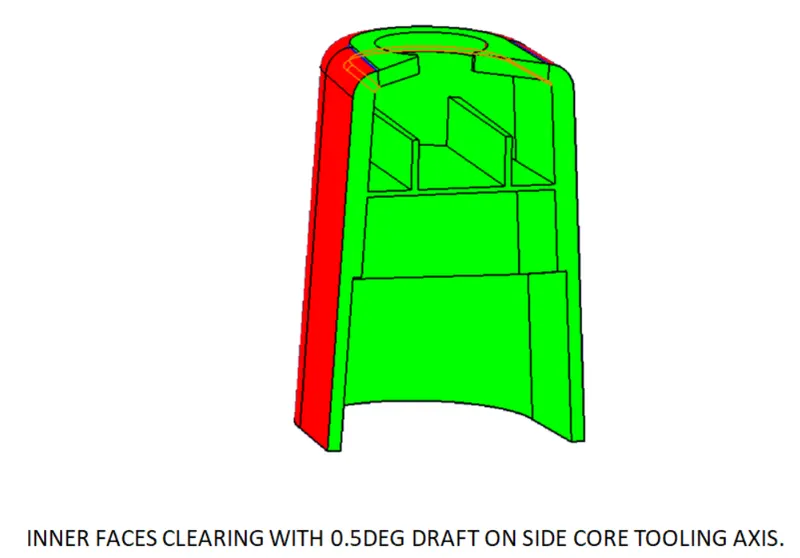
In this model we have a tooling axis in the perpendicular direction to the entire door trim that is y-direction in the model. It is very evident that switch bezel will require a side core, so another tooling direction is made specifically for switch bezel. Apart from these two tooling axes we also have a side core tooling axis for dog house.
FEASIBILITY CHECKING :-
DRAFT ANALYSIS
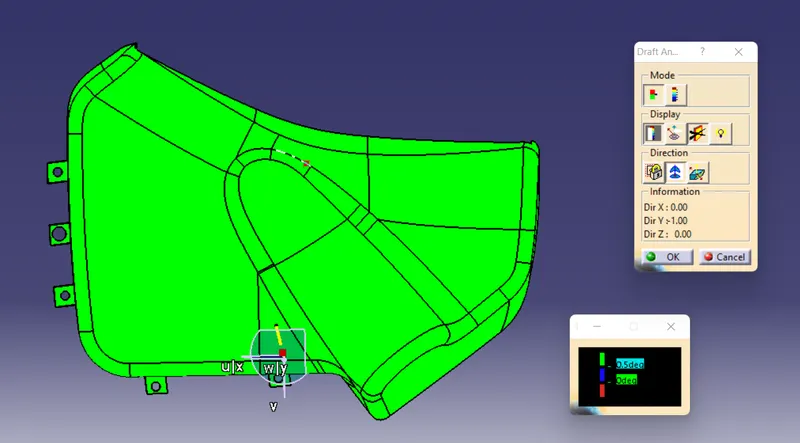
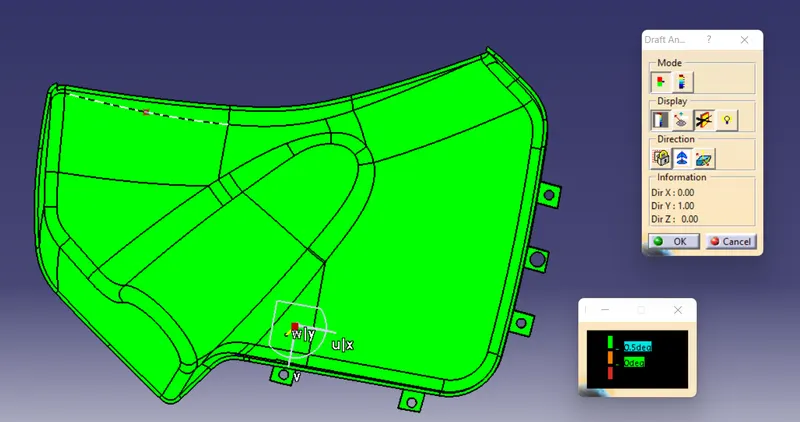
Our first step before starting the model should always be to check is the surface has enough draft that it will not create any problems while ejecting from the mold. This seems like a big task as we have to foresee something that will come at very later stage. But this is done by a small process called draft analysis. This analysis tells us whether our component will be safely ejected in the tooling axis we have provided. Some components require side core where there are under undercuts, holes or projections on the side walls, so for this we need a different tooling axis and a different analysis is required to check those areas. Draft analysis shows color codes which are defined by the user for different values which also are defined by the user. These colors help us to analysis if the component is clearing the analysis and we are good to go ahead or not. In case the component fails the analysis for class-A then we have to submit the draft analysis report to the higher authority so that the surface of the component can be improved. Failing analysis simply means that the component does not have the required draft value it must have. In case our solid model which we develop, fails the analysis at some parts then we have to correct it ourselves.
We have to make sure that our entire model is green which means it is clearing the analysis. So we have to run analysis for class-A, solid model and other B-side features as every single component, regardless of its size should be ejected safely from the core.
NOTE :- ALL THE DRAFT ANALYSIS ARE PERFORMED ON CLASS_A SURFACE FOR DESIGN VALIDATION
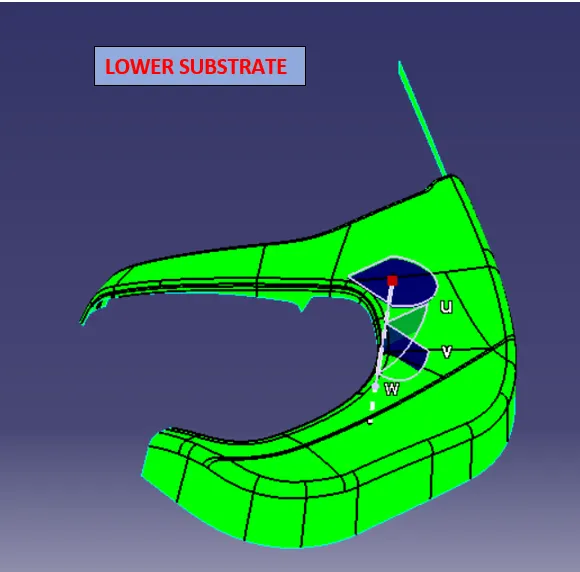
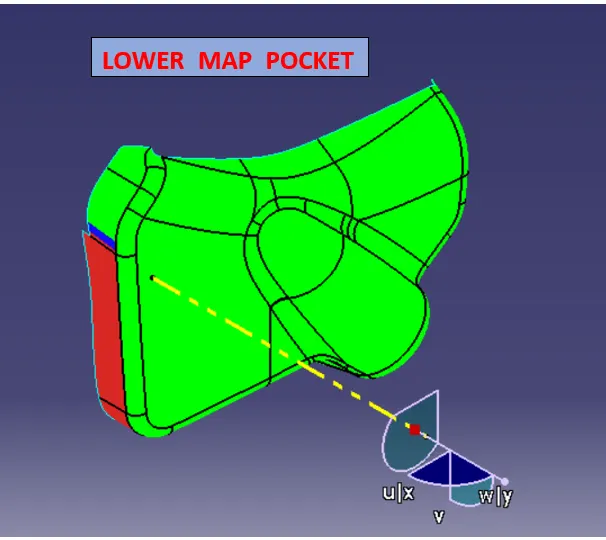
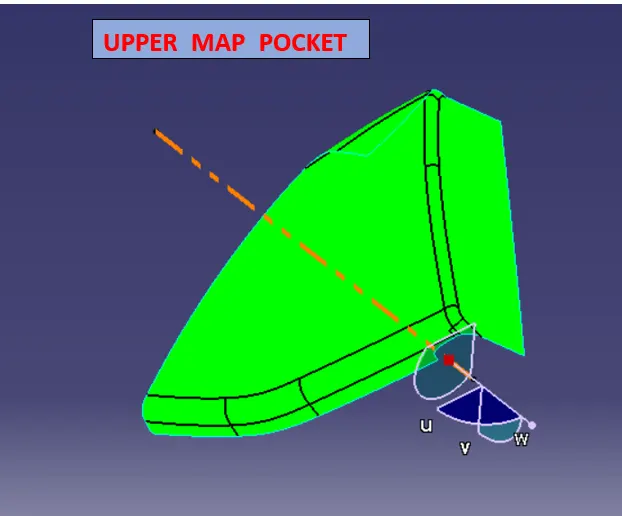
As we can see from our analysis that map holder need improvements. On industrial level in such case we cannot proceed with this class-A, but for the project we are making this model anyway. We expect this component to fail the analysis later too.
DESIGNING PLASTIC COMPONENT & CONCEPT VALIDATION
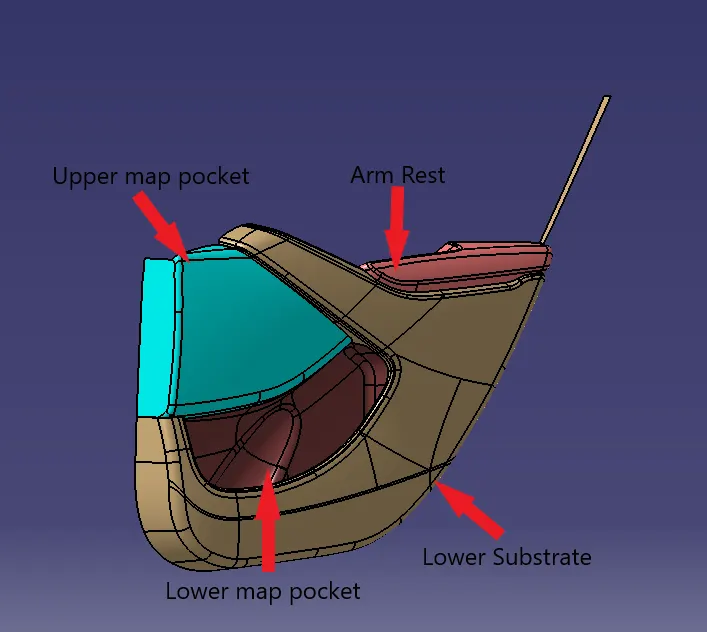
- As the entire door panel is divided into various components, we will make this plastic component in the same way. Following steps have been carried out to make the plastic component for every component:
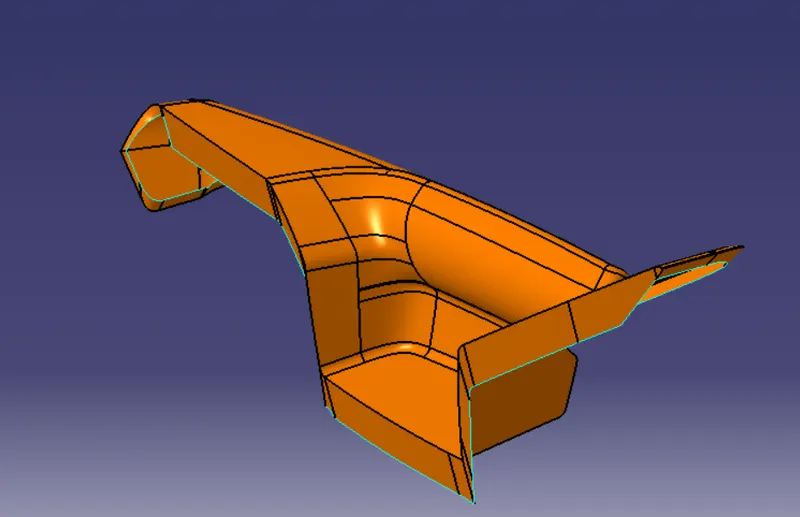
- The first step for every component was same. The given input was not a single unit but has numerous patches. These patches were joined together using join command. Thus after performing this operation we got our single class-A surface.
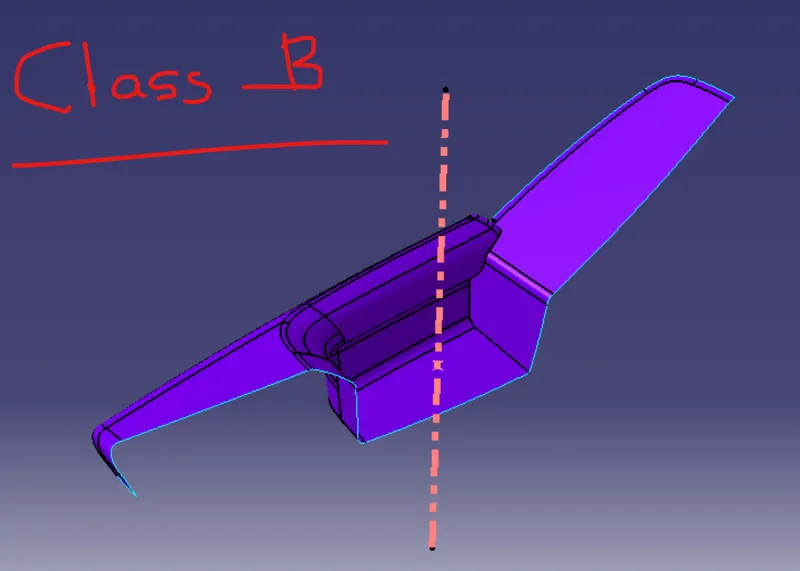
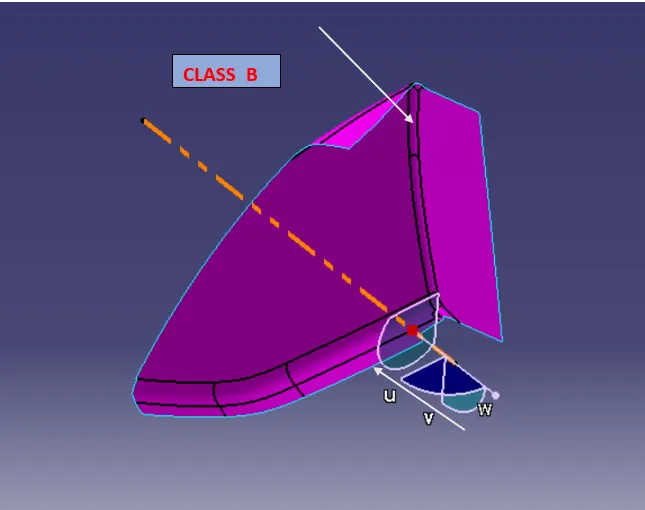
- Once we get class-A, we have to proceed to make class-B surface. Creating class-B by extracting every flat surface will be a complex process in such component. So we directly offset it by 2.5mm.
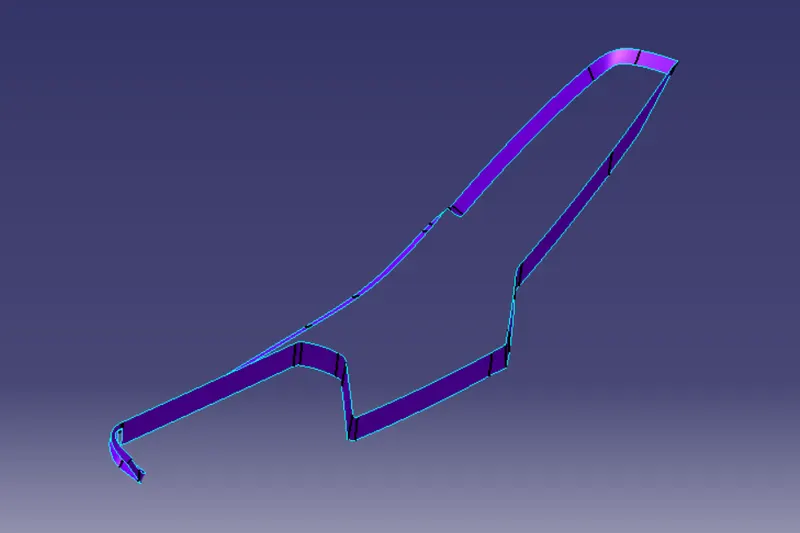
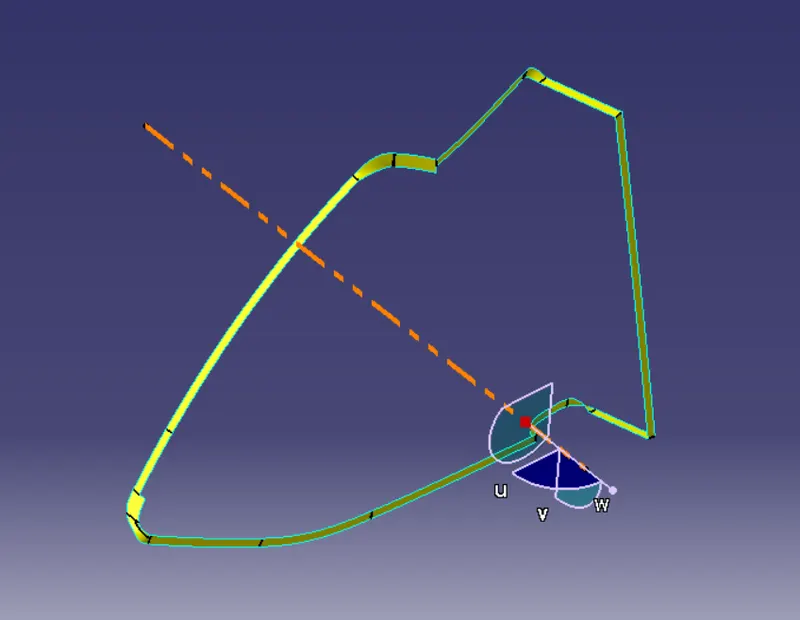
- For making class-C surface we have used sweep command ‘with draft direction’ by giving 3deg draft angle and tooling axis as direction. But at many places this did not work so we have to sweep ‘with reference surface’ at 90deg. Once that was done, the C surface was joined together using join command.
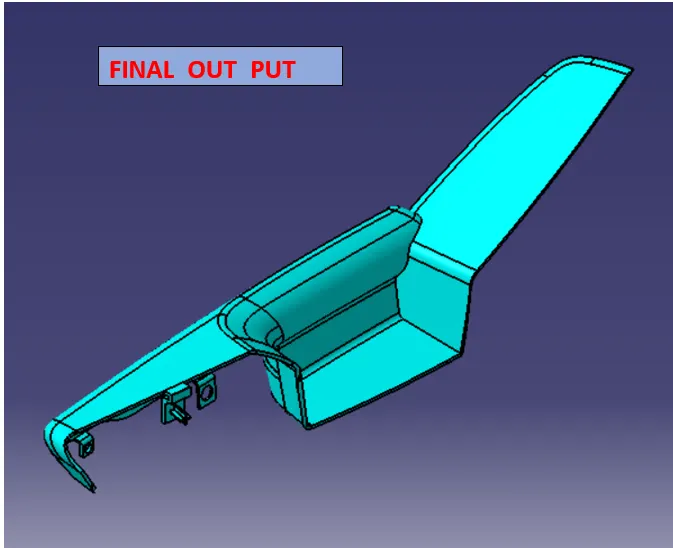
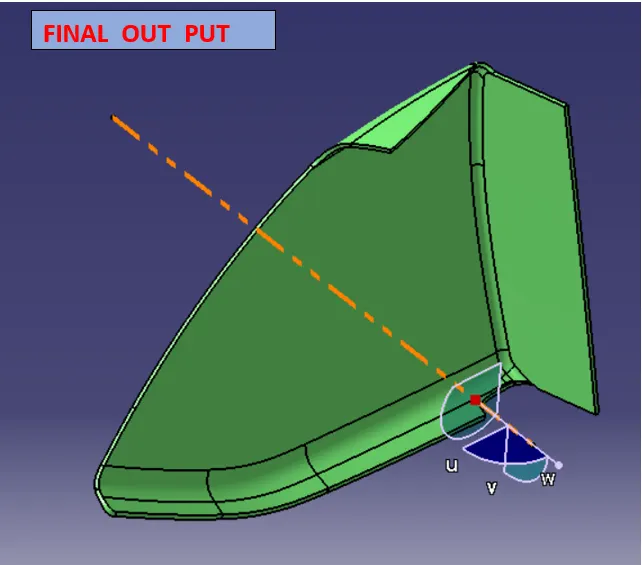
- To make a final surface model, we have to trim all the three surfaces together. And later go to part design to close the surface.HERE ARE THE IMAGES OF EVERY COMPONENT IN THE ORDER OF THE ABOVE STEPS
ARM_REST :-
CLASS_B
CLASS_C
CLASS_A&C (JOINED) :-
FINAL_PART WITH ENGINEERING FEATURE_
DRAFT ANALYSIS OF FINISHED PART :-
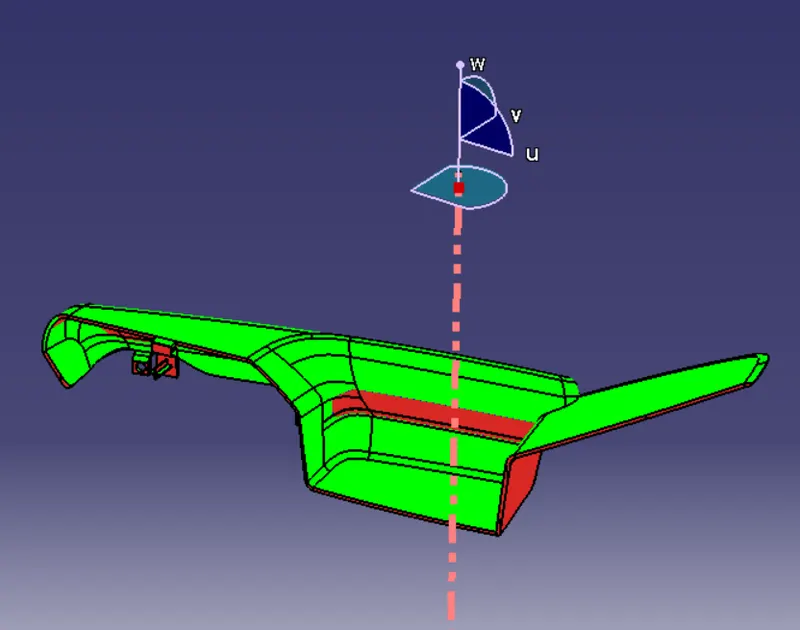
- AS THE CLASS_A WAS NOT CLEARING THE FULL DRAFT THE FINAL_PART HAS SOME DRAFT CLEARING PROBLEM .
LOWER_SUBSTRATE
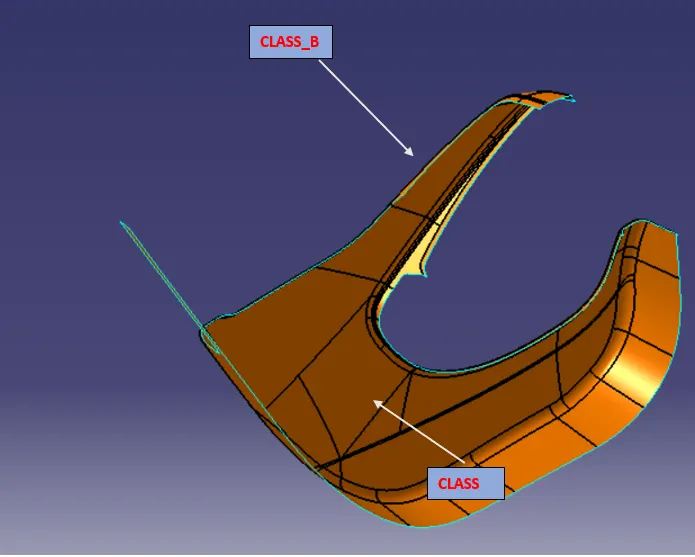
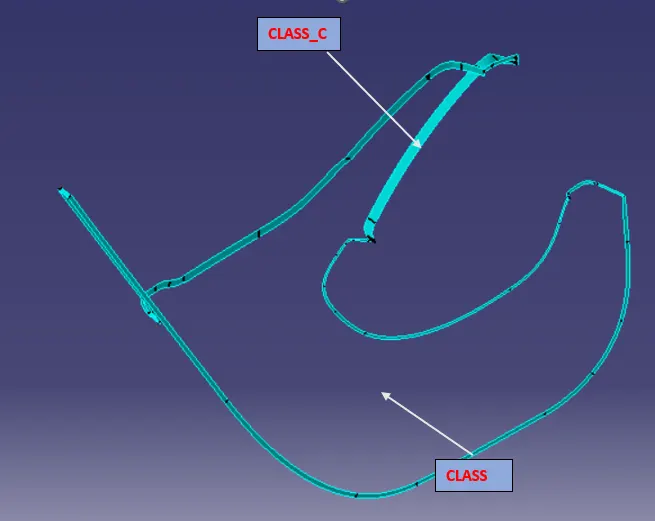
JOIN_CLASS_A AND C
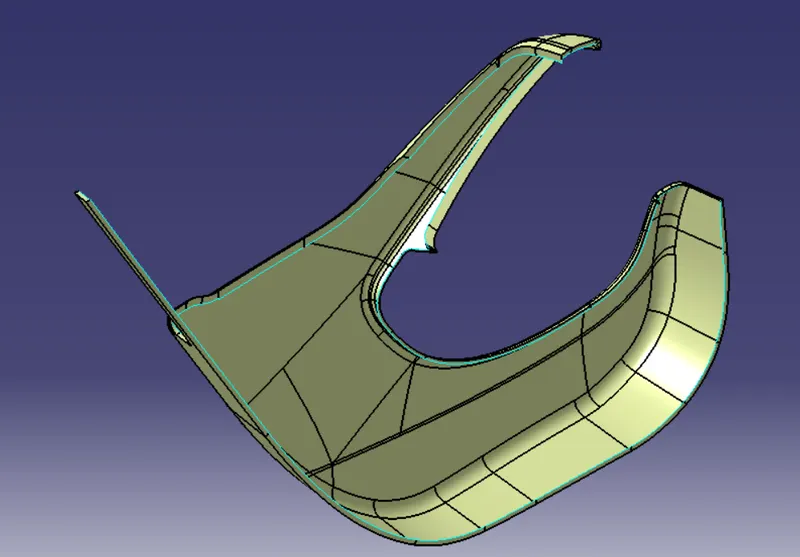
FINAL_OUT_PUT
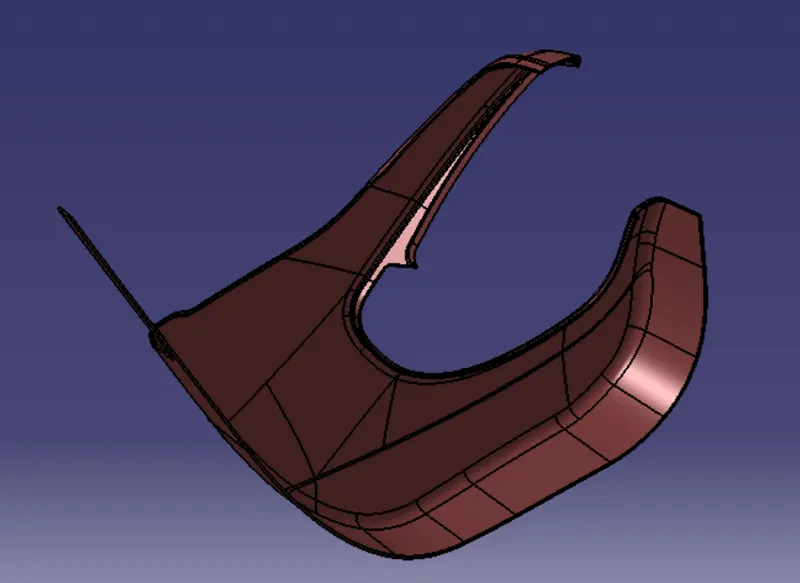
WITH_B SIDE FEATURES (ENGINEERING FEATURES {-
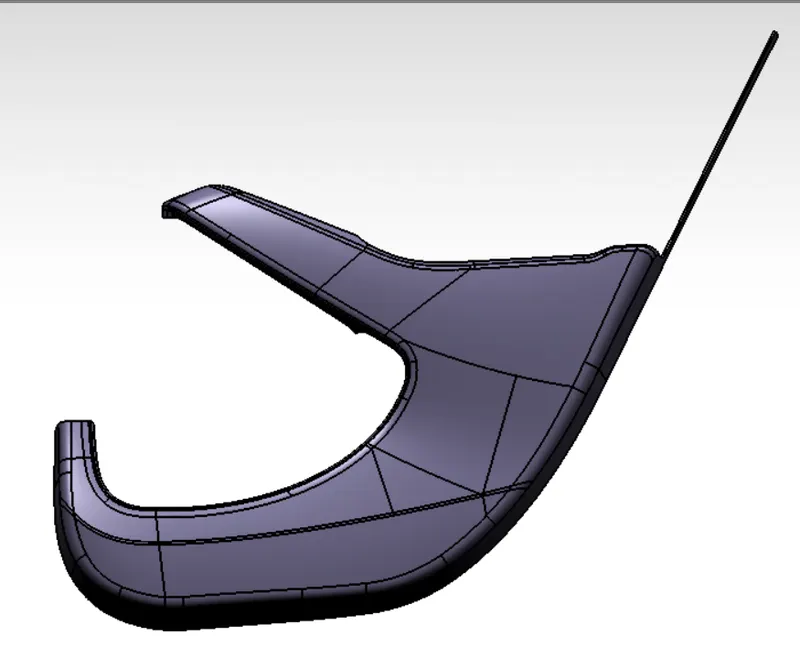
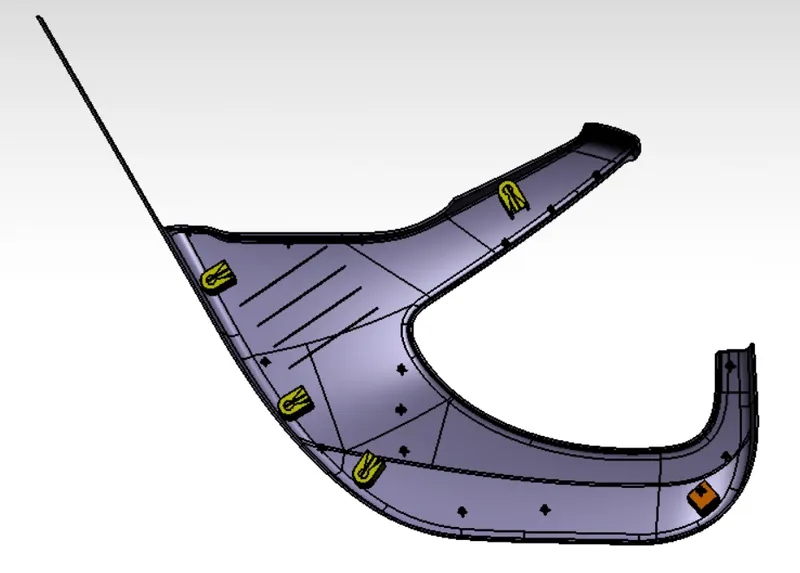
FRONT VIEW RARE VIEW
DRAFT ANALYSIS OF FINAL COMPLEAT PART_
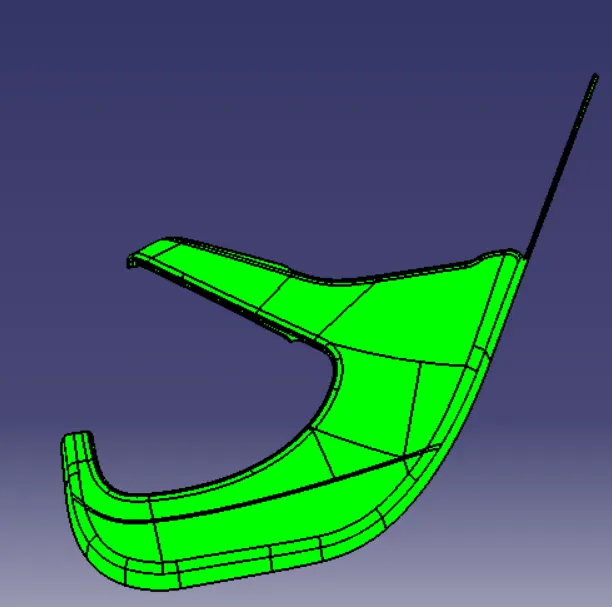
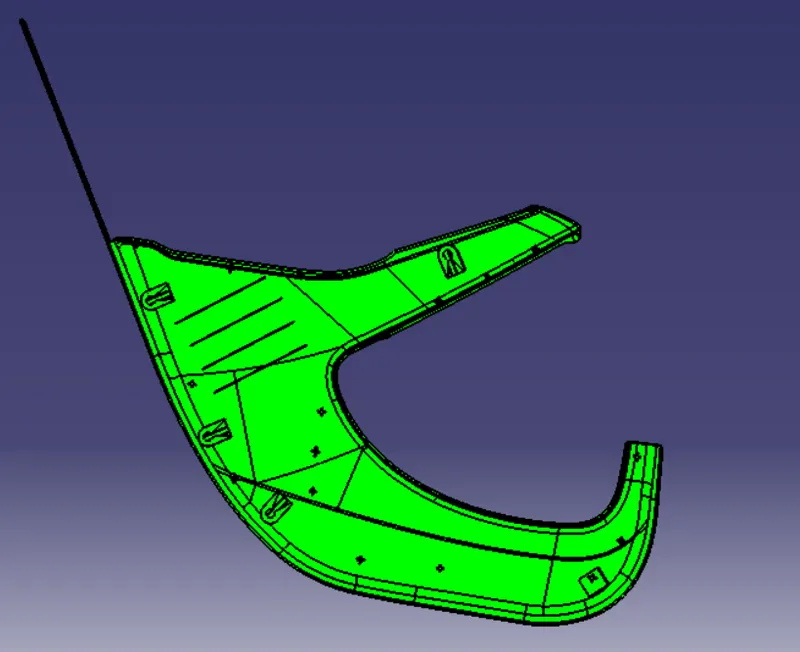
FRONT VIEW RARE VIEW
UPPER_MAP_POCKET
CLASS_B
CLASS_C
FINAL_OUT_PUT
CLOSED_BODY WITH B_SIDE FEATURES AND ATTACH MENT FEATURES
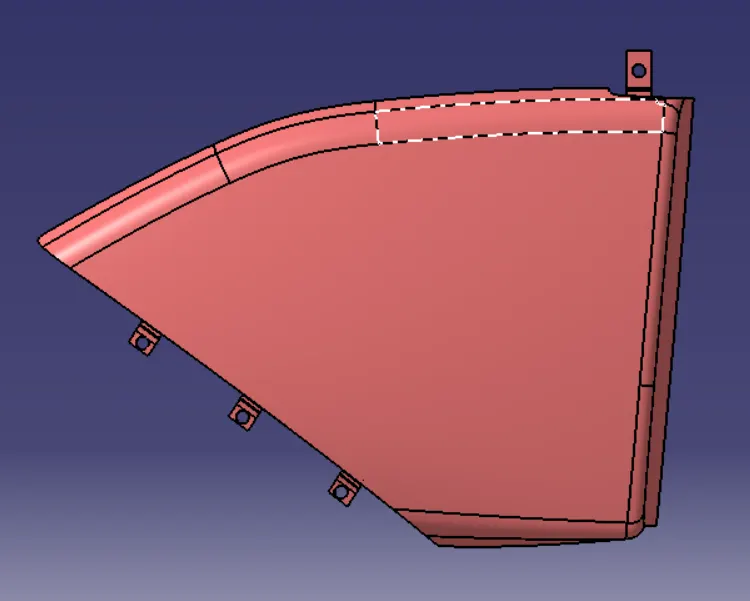
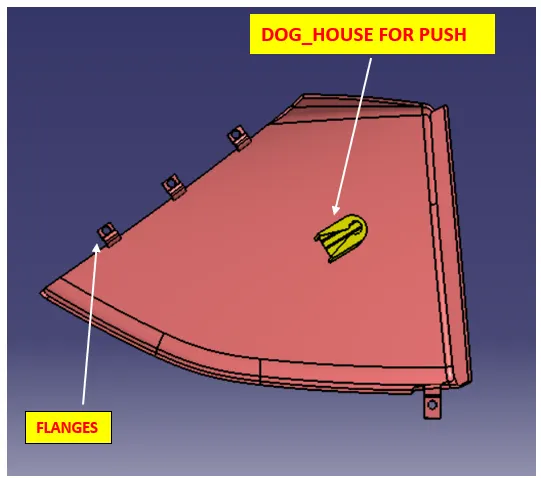
FRONT VIEW RARE VIEW
DRAFT ANALYSIS:-
FRONT VIEW
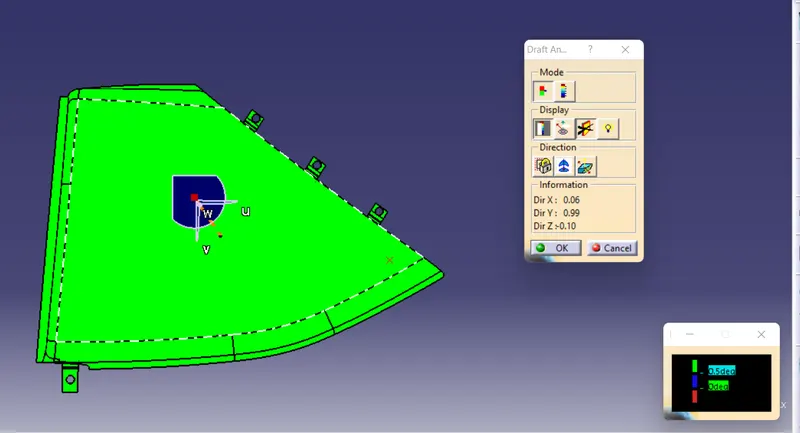
BACK_VIEW
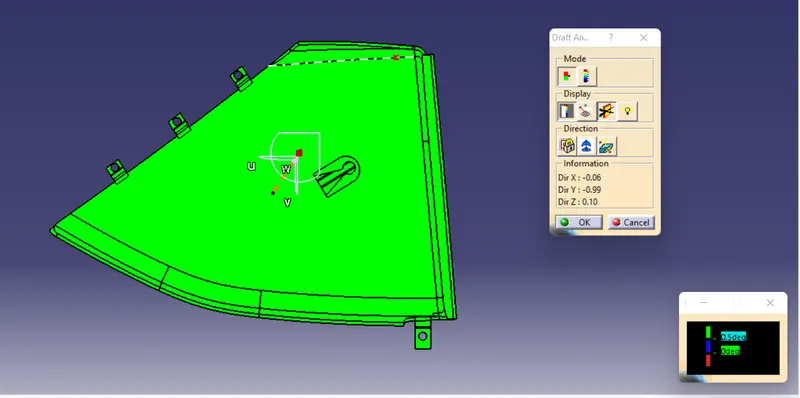
ISO VIEW
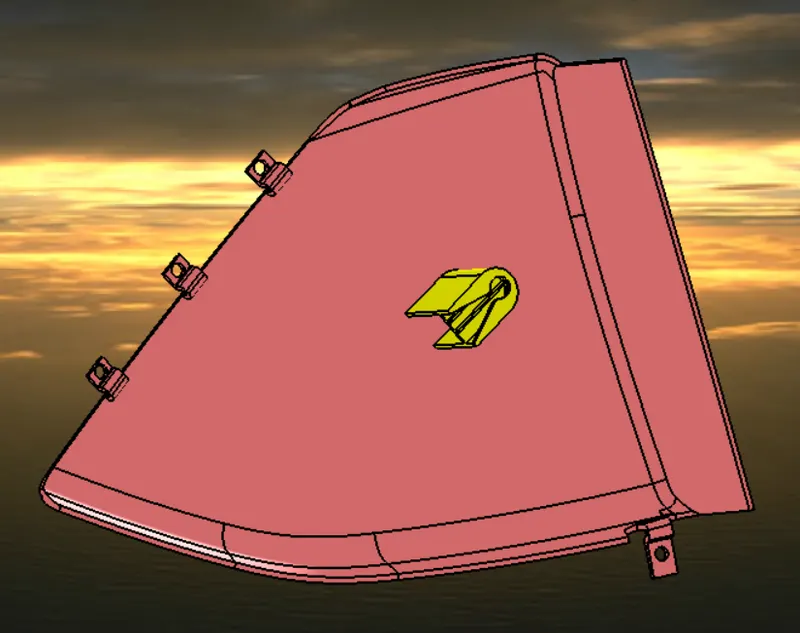
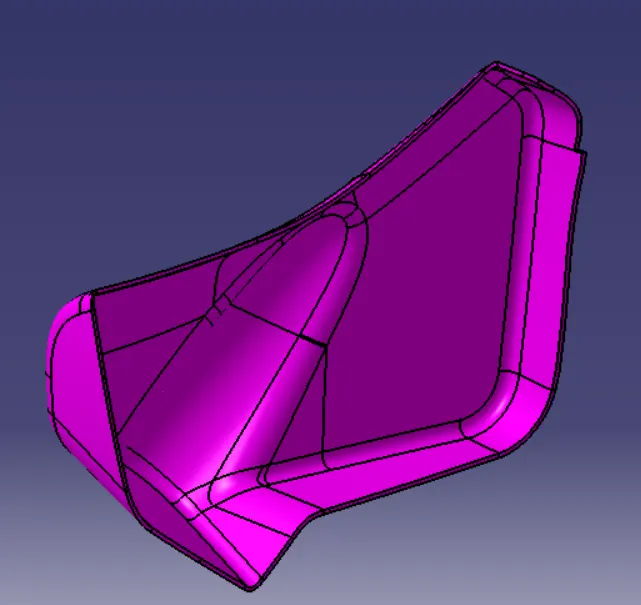
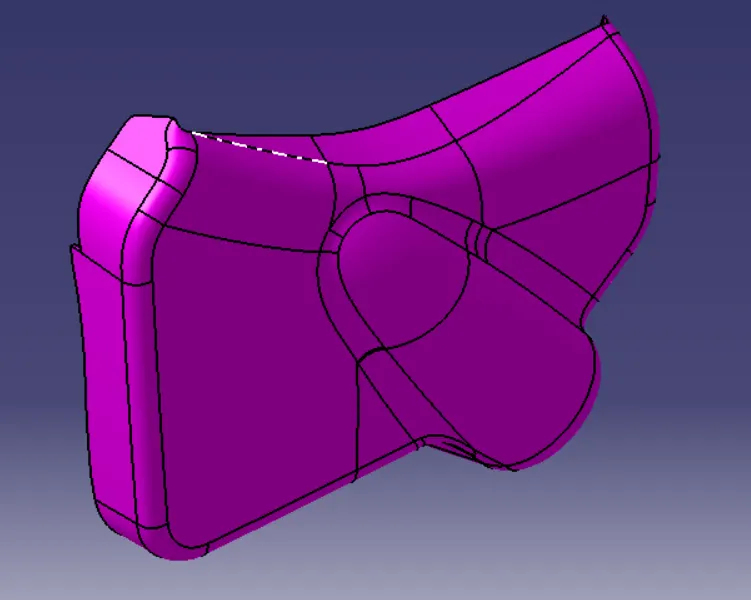
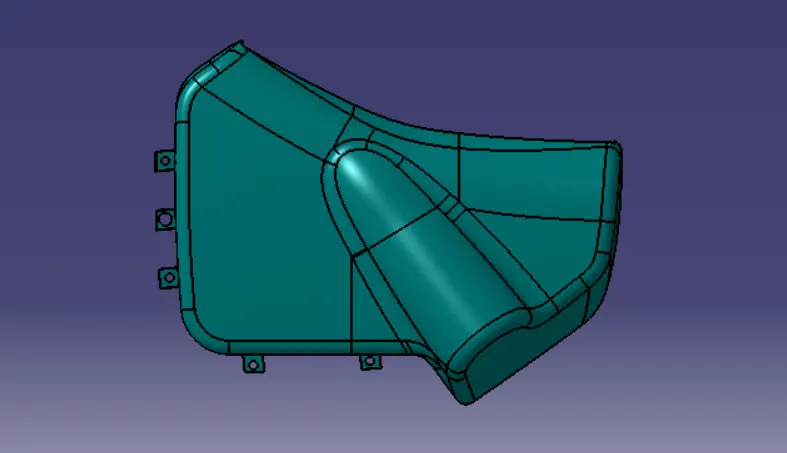
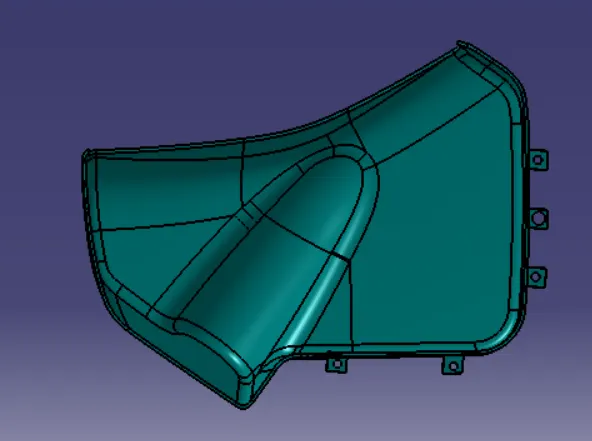
LOWER_MAP_POCKET
CLASS_B
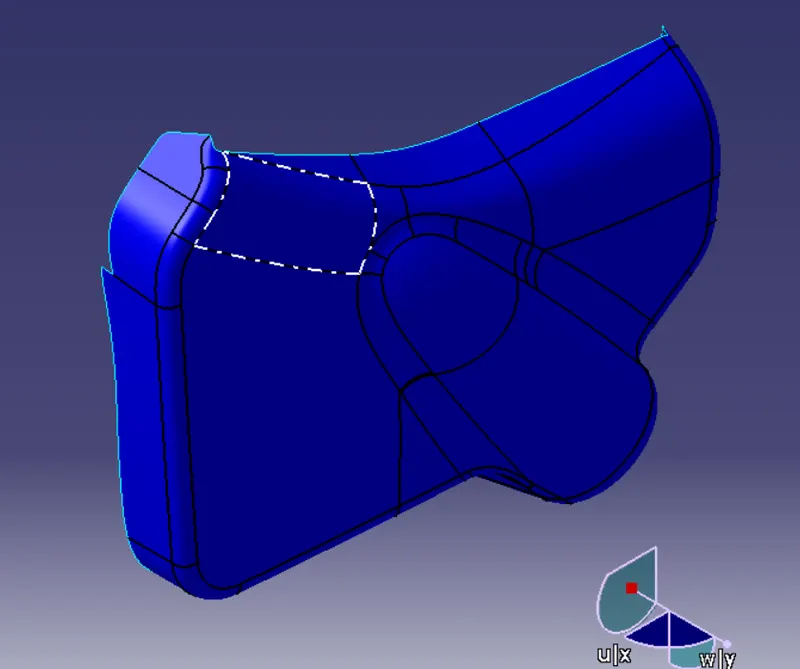
CLASS_C
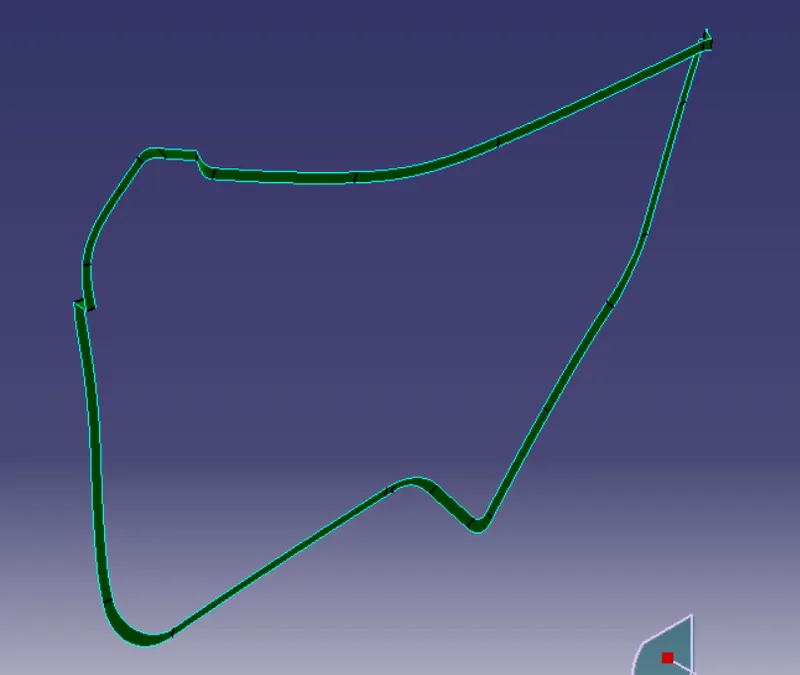
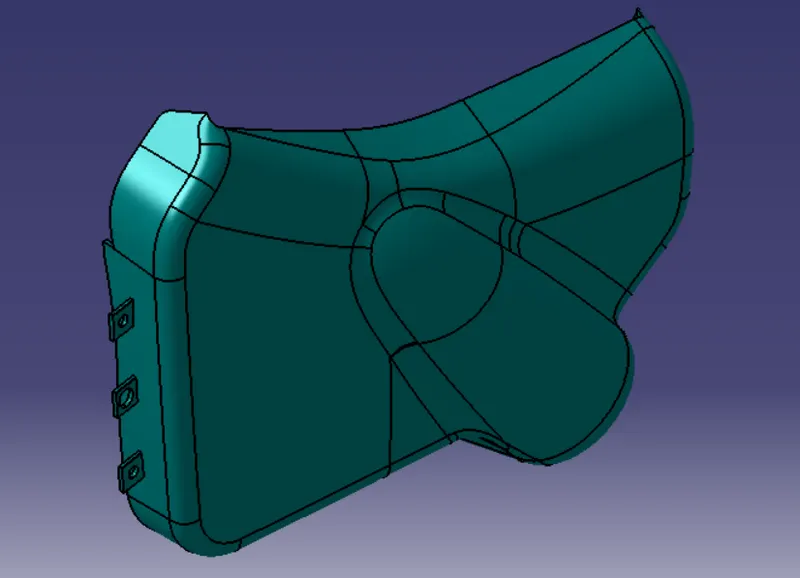
FINAL_OUT_PUT
CLOSED_BODY_WITH_ATTACHMENT FEATURES :-
FRONT VIEW RARE VIEW
DRAFT ANALYSIS :-
FRONT
BACK
ISO VIEW
DESIGNING B-SIDE FEATURES
DOOR APPLIQUES:-
SCREW BOSS: They are used for the purpose of mating two parts. They have hole in them which accepts the threaded part of the fasteners such as screws.
GENERAL DESIGN GUIDELINES FOR SCREW BOSS DESIGN:
- Draft: 5 deg on each walls.
- Wall thickness: 40% of the nominal wall thickness i.e. 0.4*t where t is the wall thickness which is 2.5mm in this case.
- Height/diameter: 3:1 steel but 2:1 is preferred.
- Radius of the fillet: minimum 0.25mm.
- Boss gussets (rib like structure giving strength to the screw boss) must meet ribs guidelines.
- Avoid merging the screw-boss into wide wall.
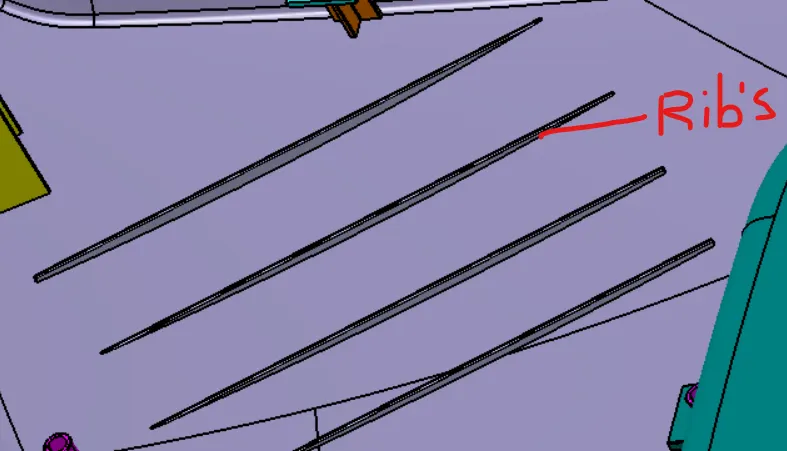
RIBS/GUSSETS: They increase the stiffness and strength without increasing overall wall thickness of the model which is not desired. They also facilitate:
- Locating and arresting components of an assembly
- Providing alignment in mating parts
- Acting as stopper or guides for mechanisms.
DESIGN RULES FOR RIBS:
- Draft: 0.5 deg per side (minimum), but this value should not be high enough that it will cause failure for other consideration. For example, more draft will result in less thickness at the top surface.
- Thickness of ribs: 40% of wall thickness or 0.4*t where t is the wall thickness.
- Height: ≤ 5 times the wall thickness i.e. 5*t
- Spacing (for more than 1 rib): 3:1- steel height/width ratio (maximum). h/w =3or2(preferred) where h is the height of the rib and w is the space between two ribs.
- Minimum thickness at the tip: 0.75
- Radius: 0.25mm max
- Ribs on opposite side of the wall should be offset
- Ribs should be connected to other structural features where possible.
- Rib root thickness should not be more than 30% of the wall thickness.
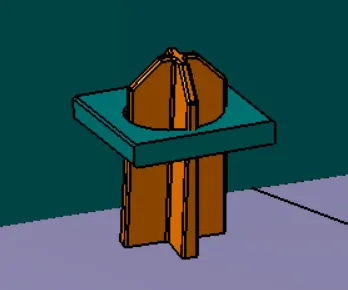
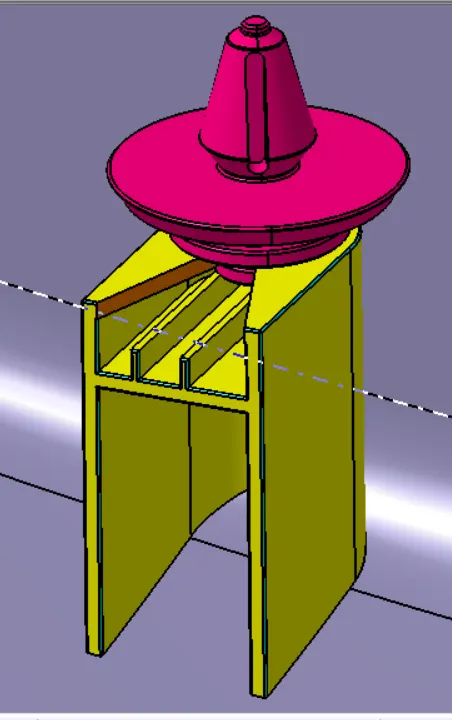
DOG HOUSE: Primary function of the dog house is to avoid sink marks. But it also helps in other things like if the mating part is to be at a greater distance then we cannot make the height of the screw boss of that greater height, thus we make dog house and mount screw boss on it. Hence it helps in solving the problem of screw boss and also it helps to have perpendicular screw boss.
GENERAL DESIGN GUIDELINES FOR DOG HOUSE DESIGN:
- Minimum height: Less than 6mm causes steel condition.
- 3:1 ratio of steel width to height. But 2:1 is preferred.
- Minimum width: 3:1 ratio of steel width to height. But 2:1 is preferred.
- Draft: minimum 1.5deg.
- Sink saver: height= 40% of nominal thickness. Width= 3.0mm-6.0mm.
- Optimal radius:25mm
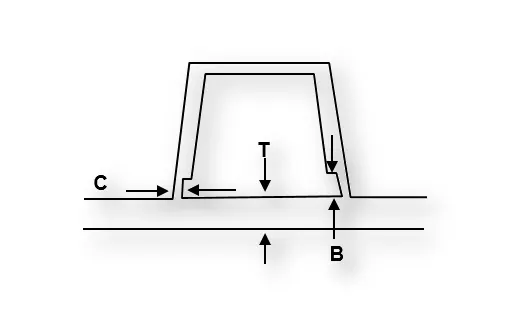
However, for this model we made a dog house which mounts push pins on it. Every above design rules were followed while making the dog house.
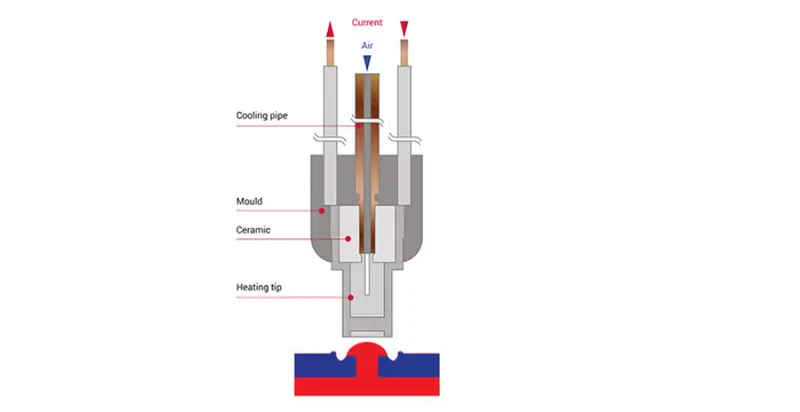
Heat stake:-
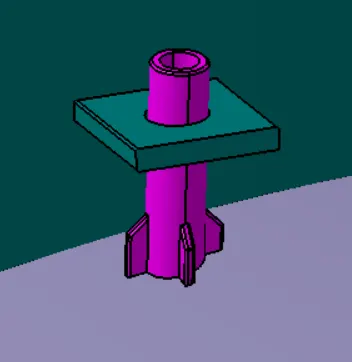
The use of heat stakes is to attach two plastic components permanently. A total of 13 heat stakes were placed at different locations on the lower substrate. One heat has been created onto the door armrest part which will be attached to the upper substrate. Following the muster section, the outer diameter of the heat stake is 7.5 mm and the inner diameter is 4.5 mm. Necessary slots are made onto other parts where heat stakes will attach together. Draft of 0.5 degrees has been given to all the heat stakes. All the heat stakes have ribs attached to them. All the ribs have 1mm thickness and 0.5 degrees of the draft. The length of the ribs is 14 x 14 mm.
Heat staking also known as thermoplastic staking is the process of joining two dissimilar materials together. In heat staking, we use local heating and cooling to raise the temperature of plastic components and allow plastic reforming to be carried out. This reforming can be used in a wide variety of applications.
locators :-
dog house :-
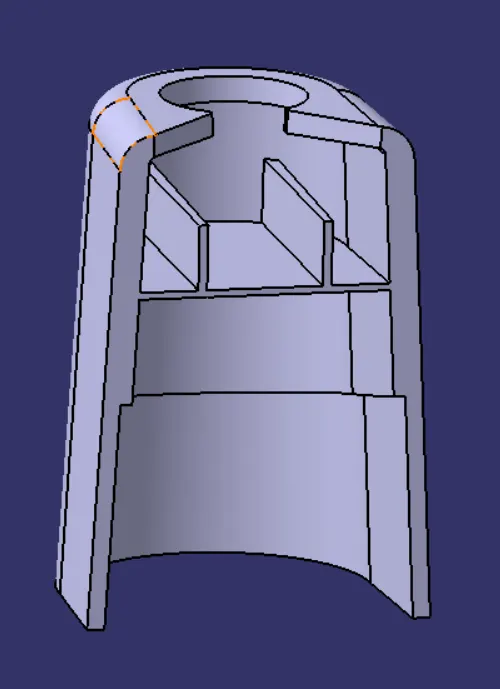
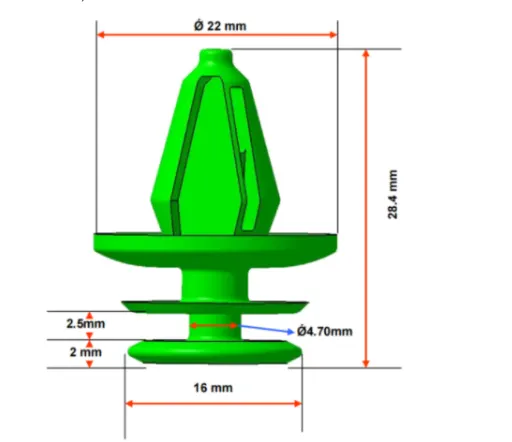
Push clips are mounted on this dog house. But as the push clips are manufactured else where and is not in our zone of concern so we have ignored the rules while making the push clips and made a general clip of similar shape in part design without following any rules.
FINAL ASSEMBLY:
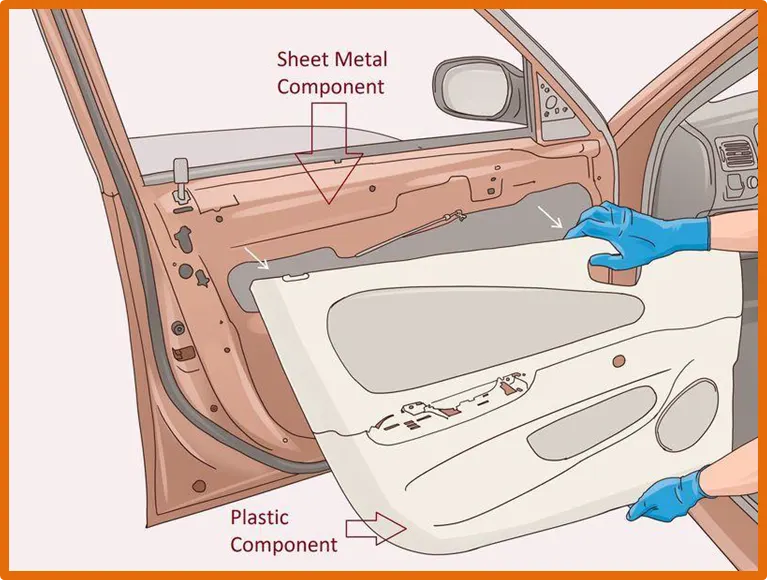
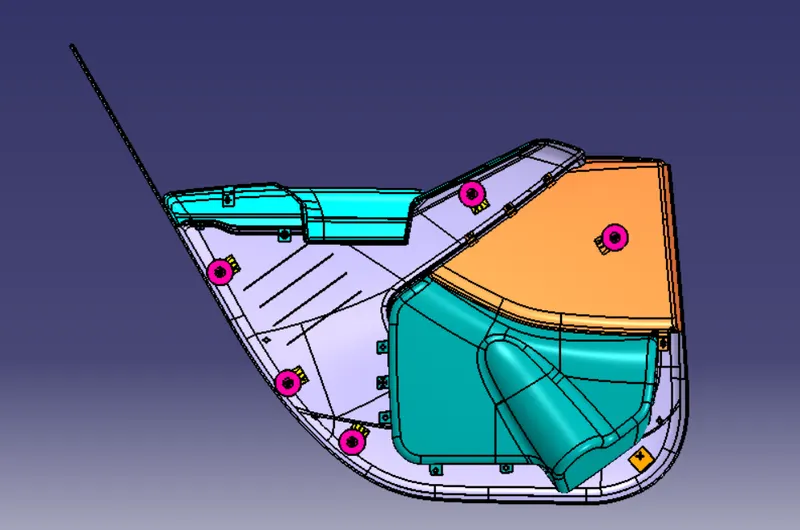
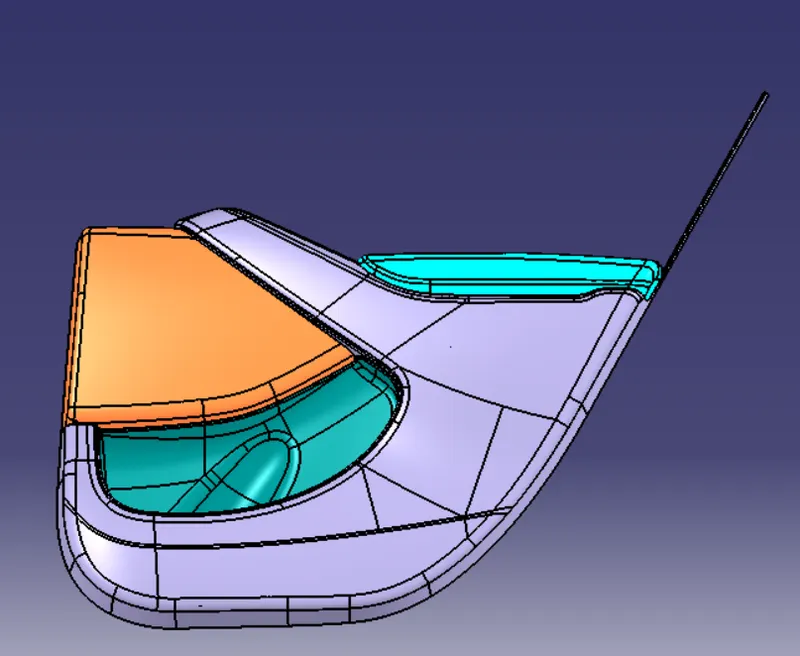
The final assembly of the door trim involved the insertion of the push clips into the respective dog house slots. Using the dog house central axis and the axis of the push pin coincident relation was given. After which, using contact constraint the push clips were made to sit in the dog house slot as required.
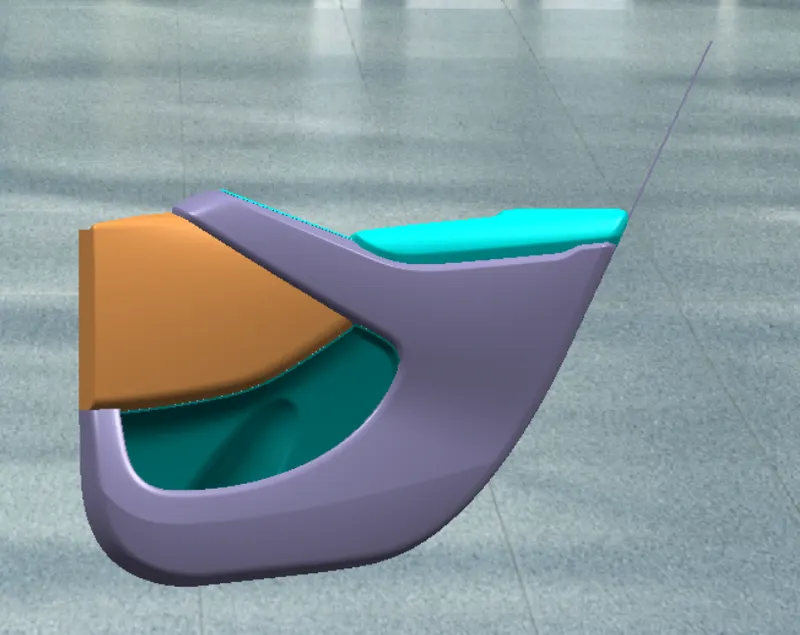
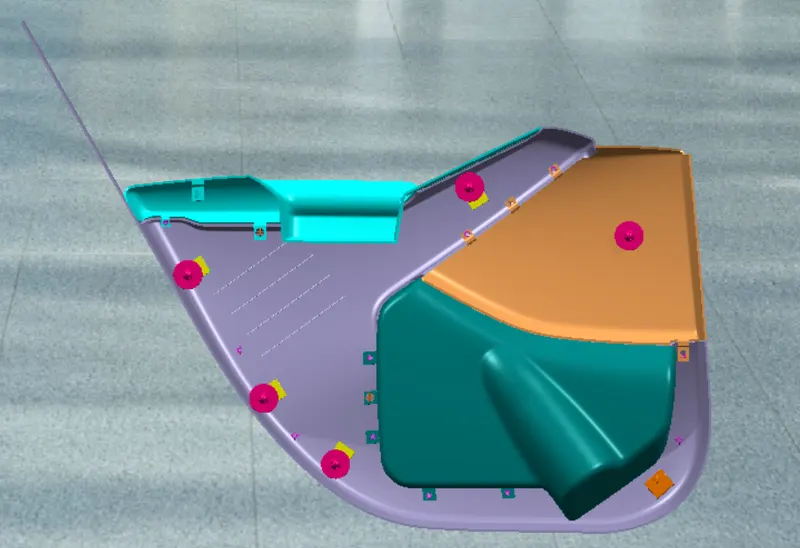
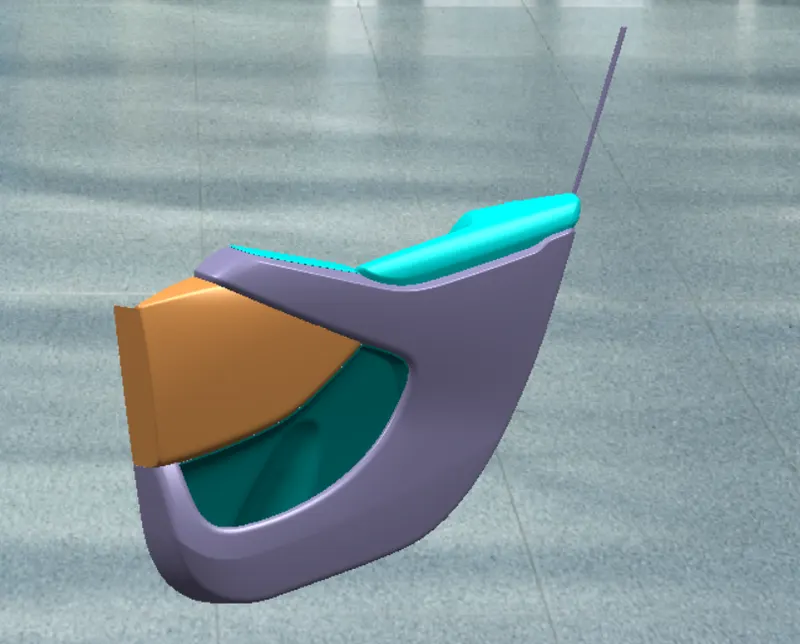
DIFFERENT MATERIAL APPLIED WITH BASIC RENDERING :-
Once the model is completed, it must be rendered for the presentation purposes. This step makes our model look attractive and presentable. Basic rendering can be done in catia and for advanced rendering we can use software like illustrator. Rendering in catia is done in following simple steps:
- Apply material to your model from the ‘apply material’ option.
- Click on render option. This has an icon of camera.
- We can manipulate the environment and background according to our need in render menu.
- Once we are done with setting all the values, render the model and save the image.
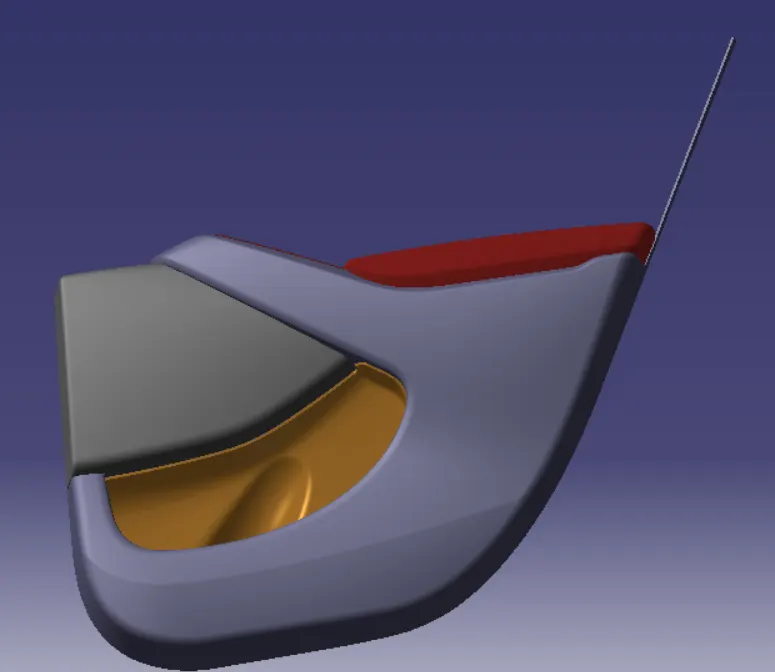
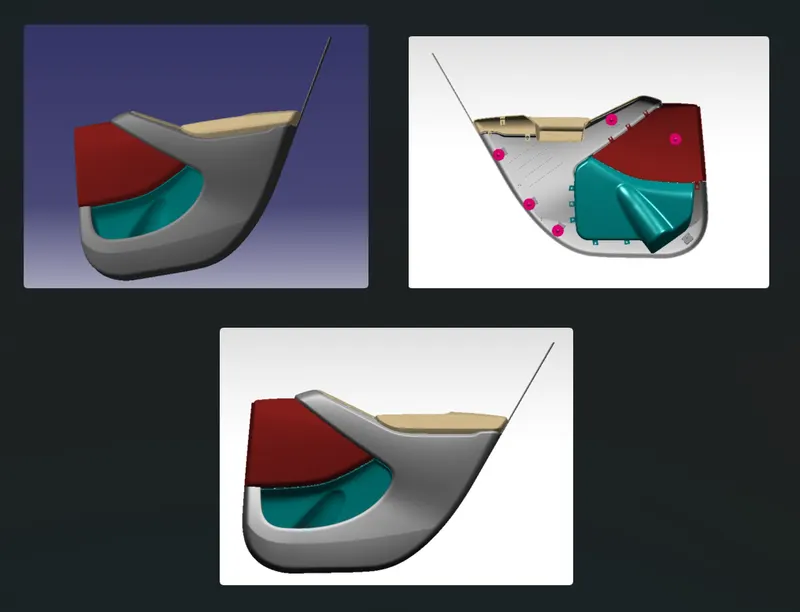
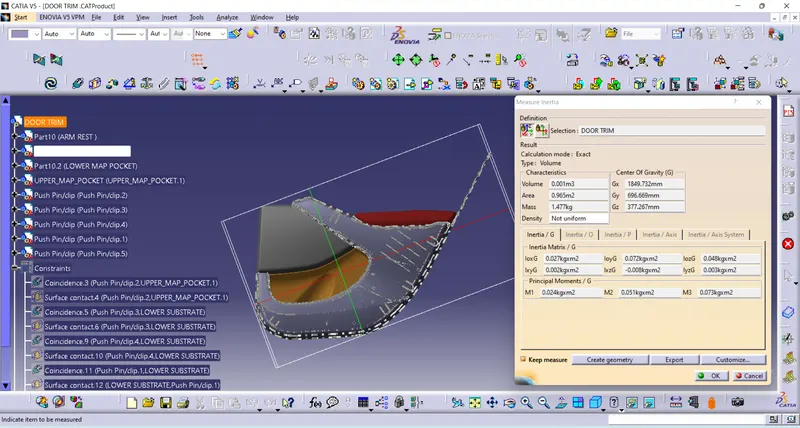
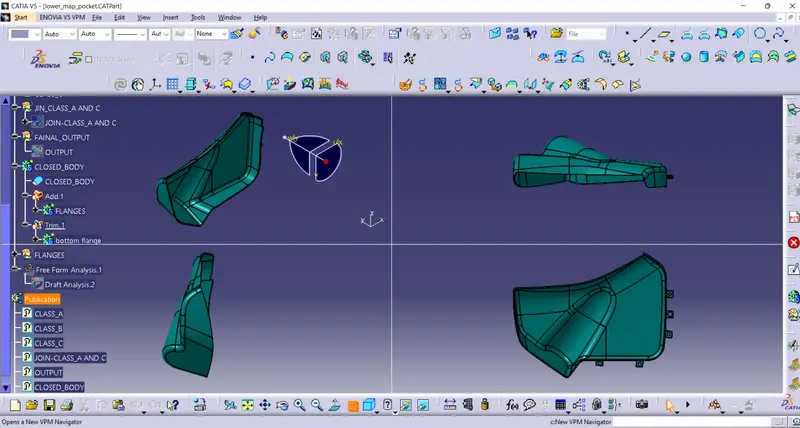
ASSEMBLY TREE STRUCTURE :-
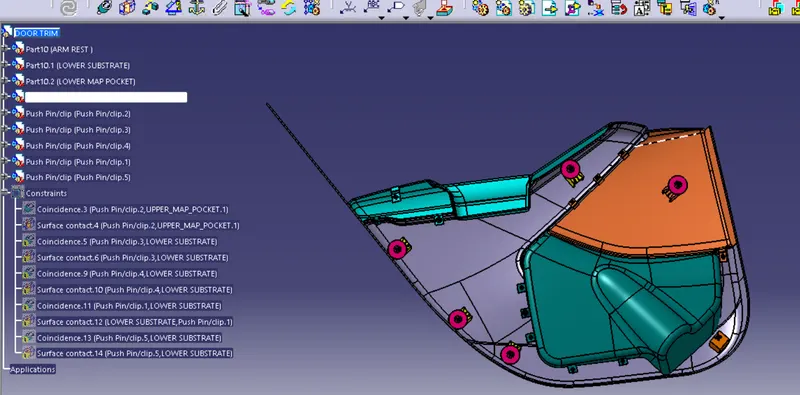
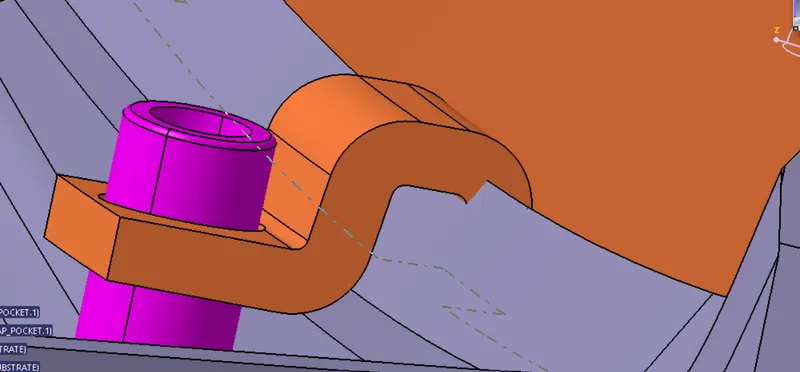
PROBLEMOCCURED :-
as the master section is fallowed the flange is intersecting with the lower substrate
CONCLUSION:
- Tooling axis for each individual part was created an draft analysis was done
- Closed surface was created for all the parts
- Attachment strategy was decide and engineering features were created
- Push clips were assembled on to the dog house and the final assmebly was created
- Plastic material was applied to all the compnents and the weight was found to be around kg 1.47KG
SUBMITTED ALL CAT FILES WITH ZIP ONE
THANK YOU.