Week 12- Final project
DOOR TRIM PANEL
Intoduction:
Design the door trim panel by the given class A surface and make draft analysis of it. By adding enginnering features to the various components by assembling the patrs. The solid plastic part was created from the Class A, class B and class C surfaces
Development of a Door Trim panel:
Creation of CAD model considering following inputs as like in OEM and tier1 companies.
- a) Class A surface
- b) Nominal thickness : Refer master sections
- c) Attachment strategy :
Find a attachment strategy for the door panel complete work. Use Push pin with Dog house for Lower substrate – Door panel attachment. Use heat stakes for part to part attachment.
Output required:
- Create thickened part using master section for reference
- Create the mounting features as per design guidelines in the industry and with master sections
- Apply material details :
- Draft analysis & Tooling analysis
- Creation of parting lines and check tooling feasibility
Overview of Door Trim Panel:
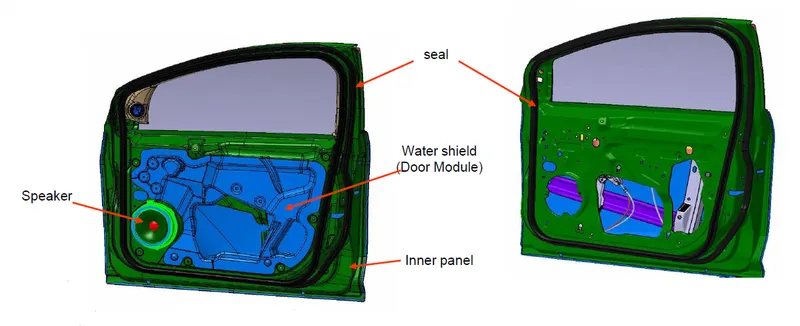
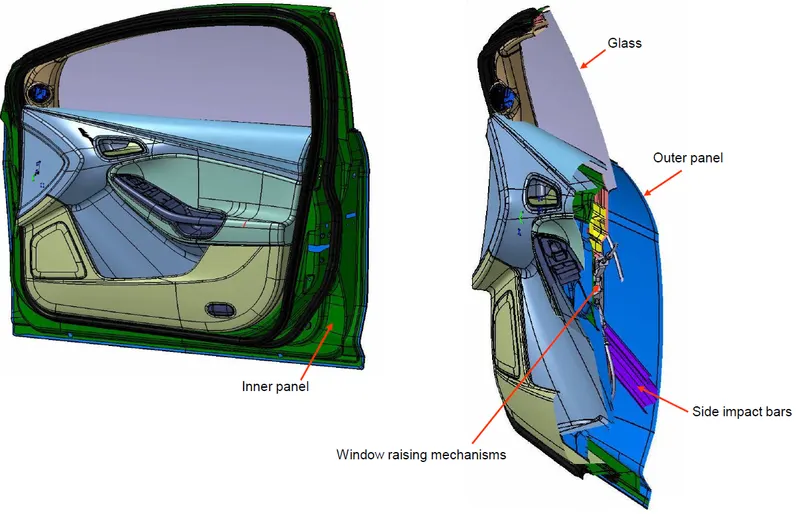
Class-A Surface:
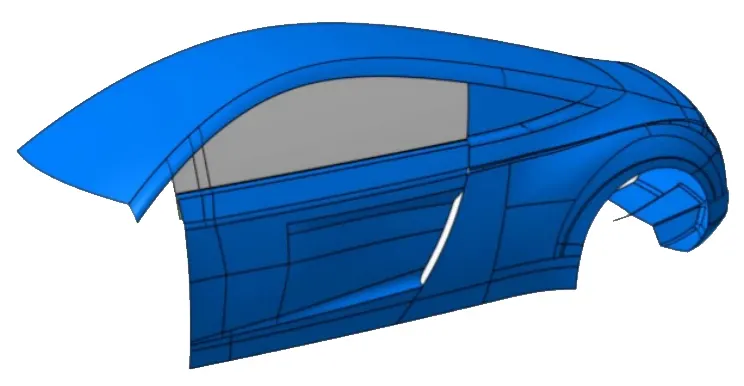
A-class surfaces are those aesthetic/ free form surfaces, which are visible to us (interior/exterior), having an optimal aesthetic shape and high surface quality. Mathematically class-A surfaces are those surfaces which are curvature continuous while providing the simplest mathematical representation needed for the desired shape/form and does not have any undesirable waviness. Products are not only designed considering the functionality but special consideration is given to its form/aesthetics which can bring a desire in one’s mind to own that product. This is only possible with high-class finish and good forms. This is the reason why in design industries Class-A surfaces are given more importance. In automotive design, a class-A surface is any of a set of freeform surfaces of high efficiency and quality. Although, strictly, it is nothing more than saying the surfaces have curvature and tangency alignment – to ideal aesthetical reflection quality, many people interpret class A surfaces to have G2 (or even G3) curvature continuity to one another (see free form surface modelling). Class A surfacing is done using computer-aided industrial design applications. Class-A surface modellers are also called "digital sculptors" in the industry. Industrial designers develop their design styling through the A-Surface, the physical surface the end user can feel, touch, see etc.
Class-B surface:
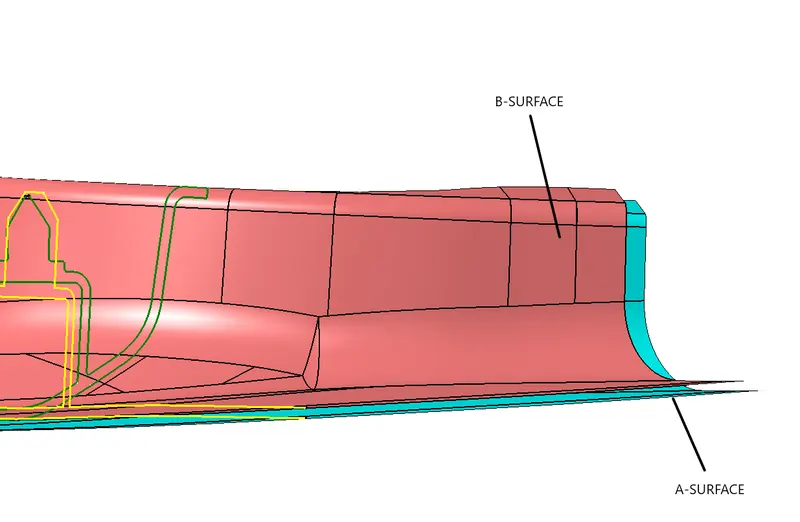
Class-B surfaces are the secondary surfaces that can be seen sometimes, but are less important, such as the inside of your glovebox, ash tray, etc. These must be smooth and "error-free" as well, but are not held to the standards that class-A surfaces are.
Class-C surface:
Class C surfaces are the backside surfaces that can have tool marks, flash and other imperfections without hurting appearance, function, etc.
Plastic Part:
When designing parts for injection molding,the manufacturing process is an important consideration. Injection molding is a process in which solid thermoplastic resin pellets are melted, injected into a mold, and then cooled back to a solid state in a new form. During both the injection and cooling stages of the manufacturing process, there are several factors that may affect the quality of the final product and the repeatability of the manufacturing process. Although it is not always possible to follow all recommendations, outlined on the following pages are some of the most fundamental guidelines when designing parts for injection molding.
Injection Molding Materials:
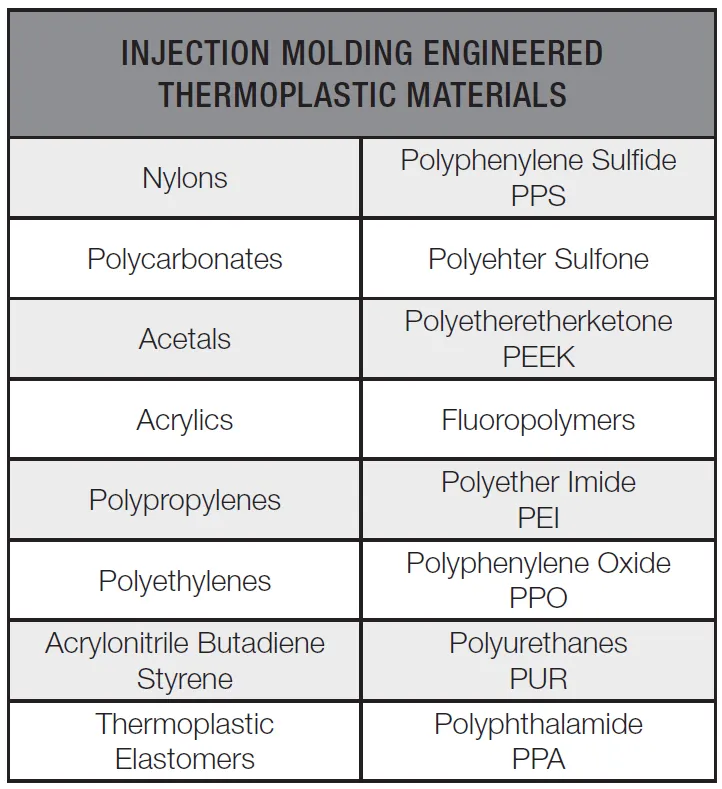
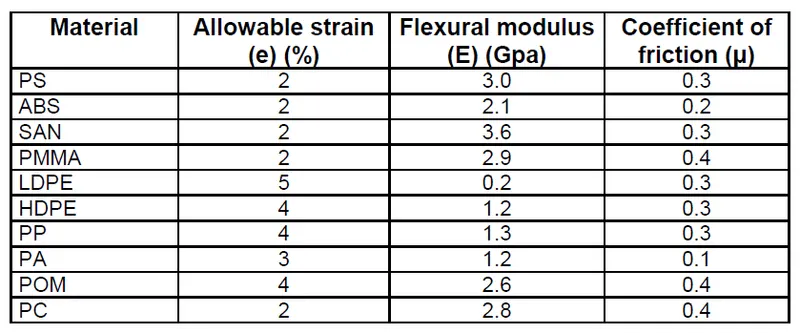
Materials Selection: Many types of thermoplastic materials are available. Selection depends on the specific application. The chart below shows some of the most common materials being used.
B-Side Features:
Boss:
Bosses are used to facilitate the registration of mating parts, for attaching fasteners such as screws, or for accepting threaded inserts.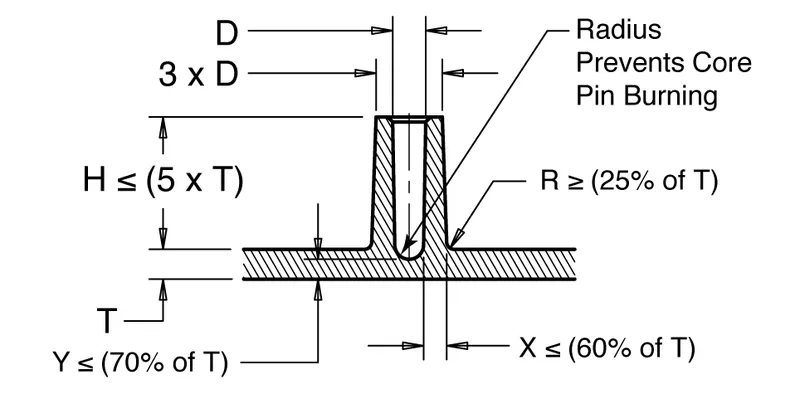
Wall thicknesses for bosses should be less than 60 percent of the nominal wall to minimize sinking. However, if the boss is not in a visible area, then the wall thickness can be increased to allow for increased stresses imposed by self-tapping screws.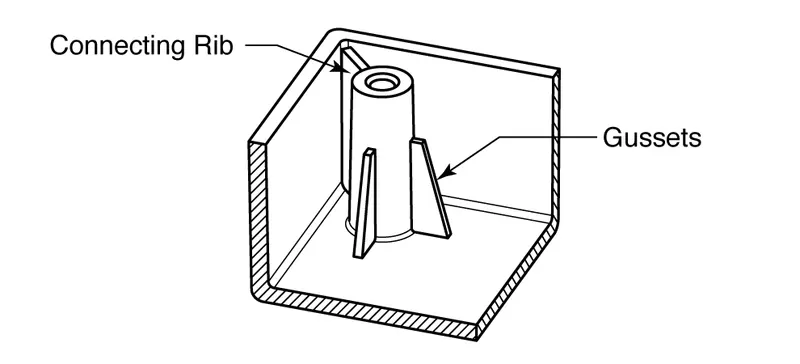
The base radius should be a minimum of 0.25 X thickness. Bosses can be strengthened by incorporating gussets at the base or by using connecting ribs attaching to nearby walls.
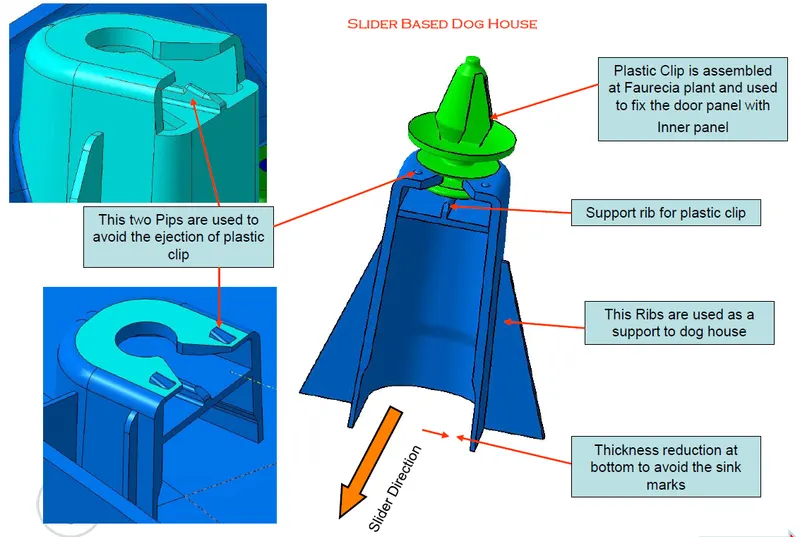
Dog House:
Dog house is an engineering feature used in plastic trim design. Dog houses are used as supporting features. Sometimes other engineering features like snaps; locators etc. are mounted on them to increase their strength. Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on a B-surface.
Dog House Design:
Dog houses are used as supporting feature.Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on a B-surface.
Doghouse design Guidelines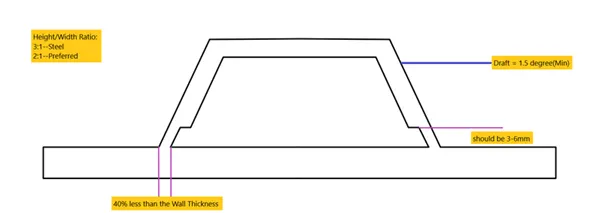
Typical Dog house Design:
4-Way Locators:
These are the locators which arrest the 4 degrees of freedom by four ribs junctioning together. These are of the following type especially used for mold designs.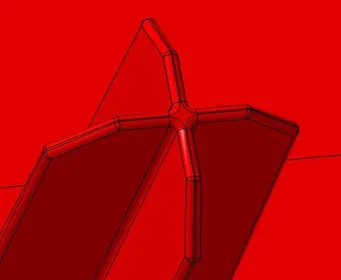
Ribs:
Ribs are thin, wall-like features typically designed into the geometry of a part to add internal support to walls or other features like bosses. In a similar fashion, gussets are support features that reinforce areas such as walls or bosses to the floor.
Ribs provide a means to economical stiffness and strength in molded parts without increasing overall wall thickness. They also facilitate:
- Locating & arresting components of an assembly.
- Providing alignment in mating parts.
- Acting as stops or guides for mechanisms.
A well-designed rib will overcome the following disadvantages:
- Increase part weight and cost proportional to the increase in thickness.
- Increase molding cycle time required to cool the larger mass of material.
- Increase the probability of sink marks.
Typical uses of Ribs:
- Covers, cabinets and body components with long, wide surfaces that must have a good appearance with low weight.
- Rollers and guides for paper handling, where the surface must be cylindrical.
- Gear bodies, where the design calls for wide bearing surfaces on the center shaft and on the gear teeth.
- Frames and supports.
Ribs design involves 5 main issues:
- Thickness.
- Height.
- Location.
- Quantity.
- Manufacturability.
Rib Geometry:
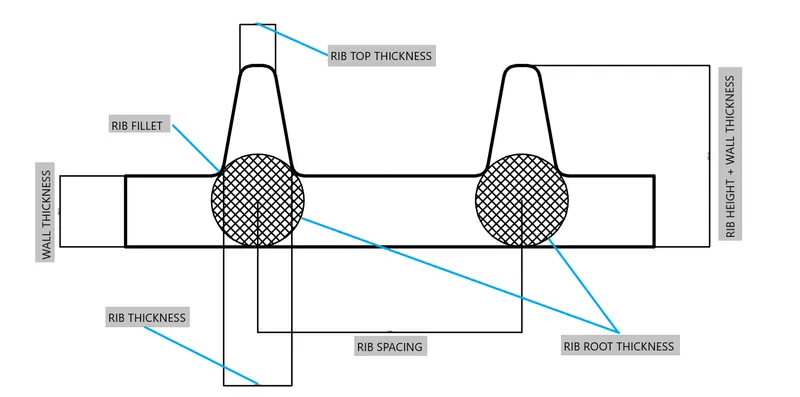
1)Rib Thickness:
Ribs should be designed to be 50-60 percent of the nominal wall thickness. Thinner does not provide much structure and may be hard to fill. Thicker ribs are tempting, but they can begin to introduce sinks on the cosmetic surface.
Bottom Rib Thickness :( 0.3 to 0.6) * Wall Thickness
Note: Top Rib Thickness should be minimum of 0.75mm.
2)Rib height:
For maximum effectiveness, rib height should be no more than three times the nominal wall thickness. Since the rib will be thinner than the wall, it may be hard to fill it if it is taller.
Rib Height= (3 to 5) * Wall Thickness.
3)Rib spacing:
Increase the number of ribs rather than their height in order to increase stiffness. Ribs should be spaced a minimum of two times the nominal wall thickness apart from one another.
Rib Height/Rib width ratio = 3:1 –steel.
Rib Height/Rib width ratio = 2:1 –preferred
4)Rib draft:
A minimum 0.5-degree draft will ensure that they release from the tool during molding.
Rib draft = (0.5 to 1) degree.
5)Rib coring:
Core thick ribs from the back or below to create a blank area and thinner rib walls. This will help mitigate cosmetic sinks.
6)Rib fillet:
Fillet at feature intersections to increase rib strength.
Rib fillet = 0.125 * Wall Thickness.
7)Rib Root Thickness:
It is the thickness at the intersection of the Rib and Wall of the plastic component.
Rib Root Thickness = (0.3 to 0.5) * Wall Thickness
Wall Thickness:
- Maintain a wall thickness of less than 5 mm because thick walls can lead to long cycle times and poor mechanical properties.
- Avoid large variations in wall thicknesses in order to simplify flow pattern and minimize variations in shrinkage that can lead to warpage.
- Avoid abrupt changes in wall thickness, as this can create stress concentration areas that may reduce a part’s impact strength. Wall thickness changes should have transition zones that reduce the possibility of stress concentrations, sinks, voids, and warp.
- Avoid gating near an area with a large variation in wall thickness because hesitation and race tracking can create non-uniform flow and shrinkage.
Snap Fits:
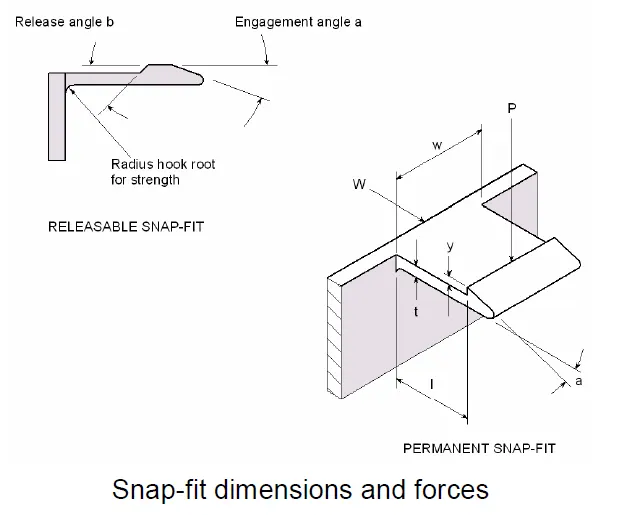
Snap-fits involve pushing a projection on one part past an obstruction on a mating part. They rely entirely for their effect on the elasticity of plastics. Generally, one part is more or less rigid while the other part is flexible or resilient. Depending on the design, the joint can be permanent or releasable. Both parts can be plastics - either the same or different types, or one part can be a foreign material such as a metal shaft or a laminated circuit board. There are three principal types of snap-fit:
- the cantilever snap-fit, also known as a snap hook, catch spring, spur, or lug.
- the cylindrical or ring snap-fit.
- the spherical snap-fit.
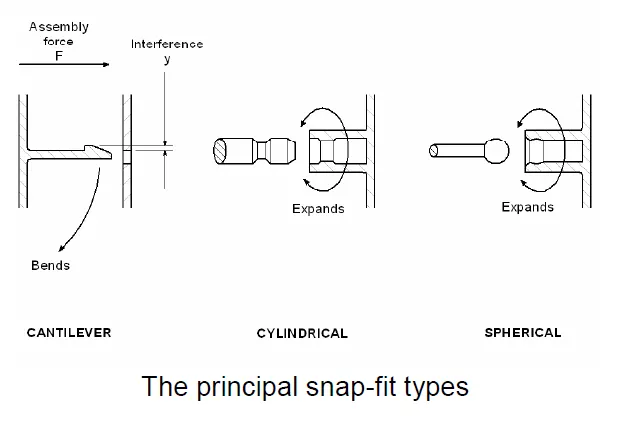
The cantilever or hook - in more detail. The cantilever type clicks or snaps into engagement when it is pushed past a catch on a mating part. The hook has a tapered face with a shallow engagement angle to help it past the obstruction. A releasable snap hook has a second tapered face set at a release angle to allow it to be removed again. The release angle is greater than the engagement angle, to make release relatively difficult. If release is too easy, the snap-fit will not act as a reliable fastener. When the release angle approaches 90 degrees, removal by pulling is virtually impossible and the snap-fit becomes a permanent joint. When the cantilever hook is pushed past the catch, it is forced to flex. The amount of deflection is equal to the interference between hook and catch, and this must be kept to a dimension that does not exceed the allowable strain for the cantilever material. The table shows approximate design data for a range of unfilled materials. The allowable strain figures are for a snap-fit that is used just a few times. If it is to be used once only, the strain figures can be doubled. The figures in the table should be taken as a guide only. For accurate design, you will need to get grade-specific figures from your materials supplier.
For a snap hook with a constant cross section, the maximum deflection Y can be worked out from this equation:
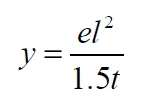
The equation assumes that only the snap hook flexes. In many cases, the moulding the face that it is attached to will also flex a little. This can be regarded as a safety factor. If the hook mounting is rigid, then you should reduce the calculated maximum deflection by a safety factor. The normal force P needed to move the snap hook through deflection y comes from this equation:
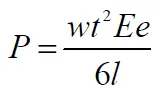
This result can be used to work out the force W needed to engage the snap fit with the catch.
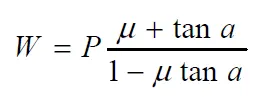
In the case of a releasable snap hook, the same formula can be used to work out the release force by substituting the release angle b for the engagement angle a. If the release force approaches the tensile strength of the snap hook, then it is likely to break as you try to release it. Similarly, the catch will shear off if its cross-section is too weak compared with either the engagement force or release force. Of course, if the snap hook is properly designed, the release force will always be greater, even in a releasable design.
Heat Staking:
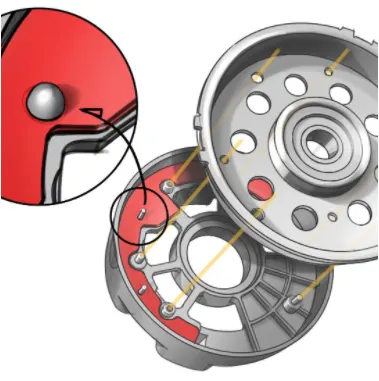
Heat Staking is a pulsed-heat process to join two or more parts out of which one at least is made of plastic. The process is to deform the plastic material using heat and force at a set process time. The bond is made by partially de-forming the plastic part in order to fix the other.
Heat Staking makes it easy to bond metal to plastic and is commonly used in high volume/low cost applications such as automotive, IT and consumer appliances.
Heat Staking Benefits:
- Similar and dissimilar materials may be joined: metal to metal, plastic to plastic, metal to plastic
- Accurate control operating within a small process window
- Local heating resulting in no damage to surrounding materials
- Processing of glass-filled materials
- No mechanical vibration
- Many heat-stake shapes are possible through custom designed tools.
Materials best suited for Heat staking:
Heat staking technology is ideal for most native and blended thermoplastics on the market today, as well as the most robust glass and/or other-filled plastics. It produces high quality results when used with any of the following materials:
- Polycarbonate (PC)
- Polypropylene (PP)
- Polystyrene (PS)
- Acrylonitrile butadiene styrene (ABS)
- Nylons (GFN or Nylon 6/6)
- Ultem (GFN or Nylon6/6)
This makes heat staking ideal for heat staking LED Stamped Arrays or LED Flex Circuits into the plastic housings for OEM automotive and aerospace industries. Heat staking is also the preferred process in many medical device assembly applications for attaching adhesive patches to wearable glucose monitor devices and wearable medicine dispense devices versus the more brittle feel of an ultrasonic welded patch against the patient’s skin. The ability to also easily transition to multiple assemblies per machine cycle makes heat staking a very desirable and controlled production equipment option versus other technologies.
When looking for heat staking plastic assembly machines and tooling, be wary of very inexpensive options – cheap or “low-cost” machines cannot be expected to maintain their temperature and motion consistently throughout the entire production run. Heat staking machines need to operate at a precise temperature, motion and force to ensure the “sweet spot” is maintained for optimum heat staking results, which occur below the thermoplastics melt temperature to maintain the most effective and repeatable assembly process.
Draft Analysis:
- The draft analysis command enables you to detect if the part you drafted will be easily removed. This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
- The maximal draft analysis accuracy is 0.01 deg. According to the graphic card performance, this accuracy can be debased.
- The different mapping analyses of the same surfaces cannot be displayed simultaneously, even if you have set the mapping analyzes in no show. You need to visualize them one after the other.
Sequence of Operations to generate CAD Model of a plastic component:
- Extracting the input Class-A surface into different parts of Assembly.
- Looking for defects in Class-A surface.
- Improving Class-A surface by patching defects.
- Improving Class-A surface as per Master section.
- Creating Tooling Axis.
- Creating Class-B surface.
- Creating Class-C surface.
- Creating a Closed Body.
- Creating Dog House as per Master Section and OEM standard design Rules.
- Creating Locator as per Master Section.
- Creating Ribs as per requirement.
- Draft Analysis.
- Adding Draft as per requirement.
- Creating Side core Tooling Axis.
DESIGNING OF PLASTIC COMPONENT FOR GIVEN DOOR TRIM PANEL CLASS-A SURFACE:
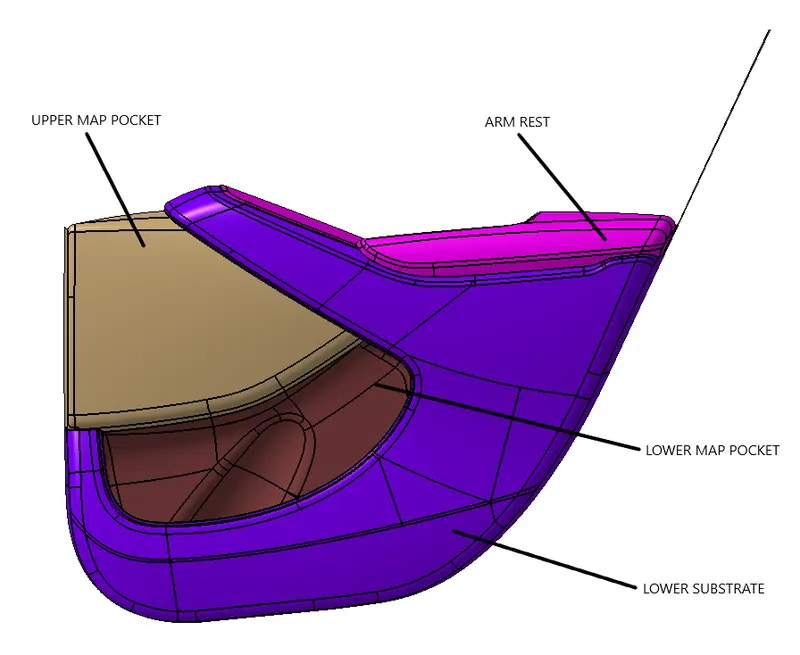
Door Trim Panel consists of following Components.:
- Door Arm-Rest.
- Upper Map Pocket.
- Lower Map Pocket.
- Lower Substrate.
- Upper Substrate.
- Flanges.
- Heat stakes and Dog Houses.
- Snap Fits.
Extracted Surfaces:
1.Door Arm Rest:
In the front of the car, a central armrest, which commonly folds away based on user preference, will also often include a storage compartment and sometimes even cup holders. Some also provide the location for controls for non-essential functions of the vehicle, such as climate control or window motors.
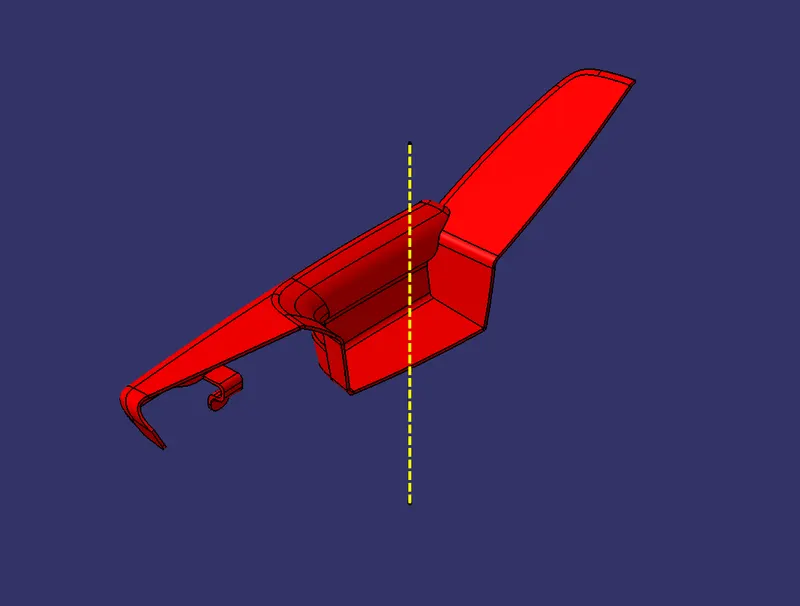
Tooling axis:
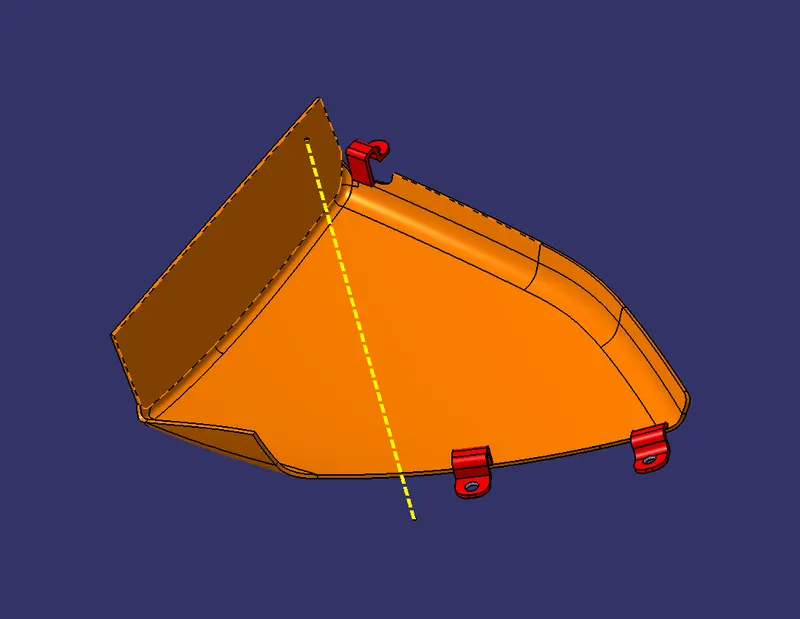
In CATIA, the tooling axis is an essential parameter when working with surface design. The tooling axis defines the direction in which a tool, such as a milling cutter or a trimming tool, will move when interacting with a surface. It is used to control the orientation and movement of the tool during operations like machining or trimming.
To set the tooling axis in CATIA during surface design, you can follow these steps:
-
Open the CATIA software and access the surface design workbench.
-
Create or open the surface on which you want to define the tooling axis.
-
Select the surface or surfaces that require a tooling axis. You can use the selection tools available in CATIA to choose the desired surfaces.
-
Once the surfaces are selected, go to the "Surfaces" or "Tools" menu and look for the "Tooling Axis" option. It may be located in different places depending on the version of CATIA you are using.
-
Click on the "Tooling Axis" option, and a dialog box or a toolbar will appear, allowing you to define the tooling axis.
-
In the tooling axis dialog box or toolbar, you will have options to specify the axis direction. You can typically define the axis using various methods, such as selecting a vector, specifying angles, or aligning with an existing reference element.
-
Choose the desired method to define the tooling axis direction and provide the necessary inputs. CATIA will display a preview of the tooling axis orientation on the selected surface.
-
Once you are satisfied with the tooling axis orientation, confirm your selection, and CATIA will set the tooling axis for the selected surfaces.
Draft analysis:
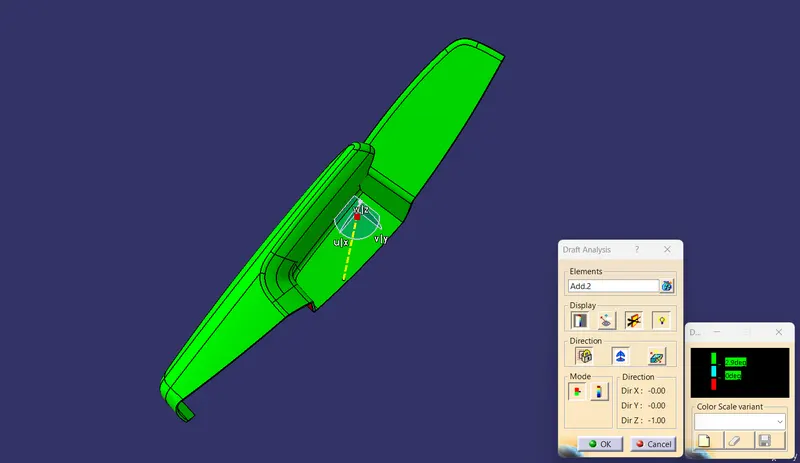
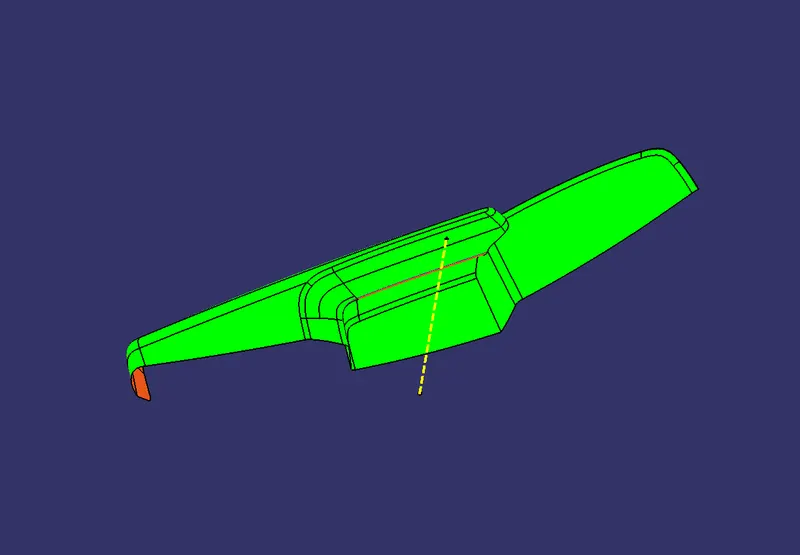
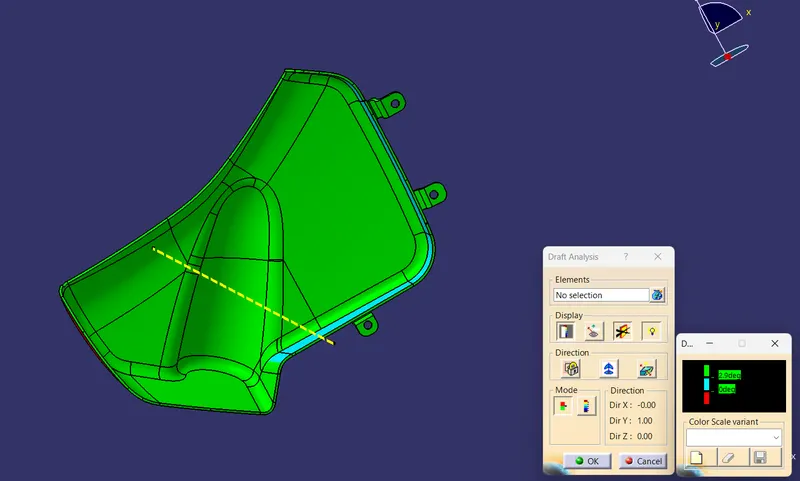
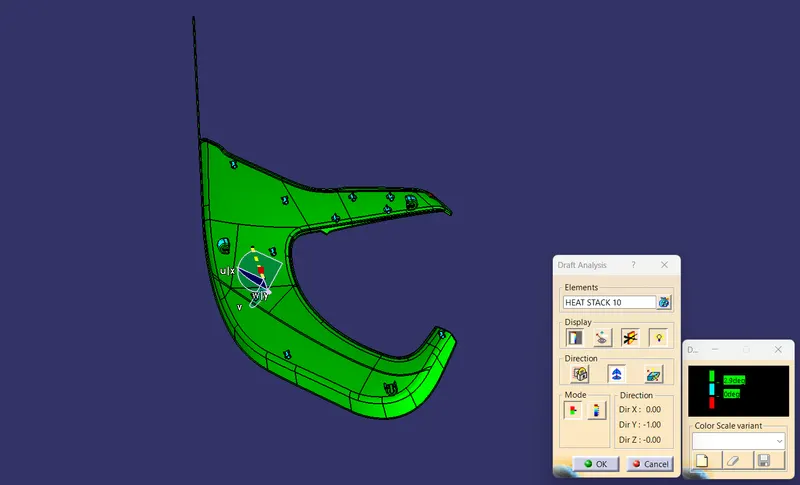
This type of analysis is performed based on colour ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values. The draft analysis button within CATIA V5 will help you quickly gather the draft angle on multiple surfaces without the need for tedious manual measurements. You need to take into account the behaviour of the plastic as it is injected and as it cools. You also need to think about how your part will be removed from the mould. CATIA V5 has special features for making this process easier.
Drafting analysis for Arm Rest:
Views:
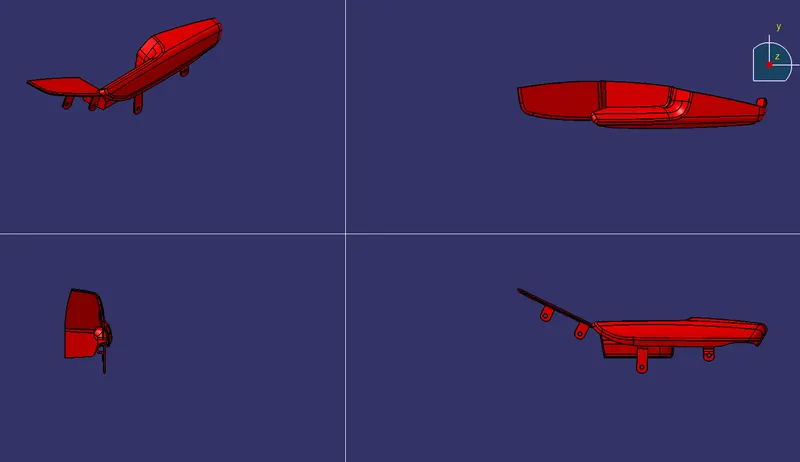
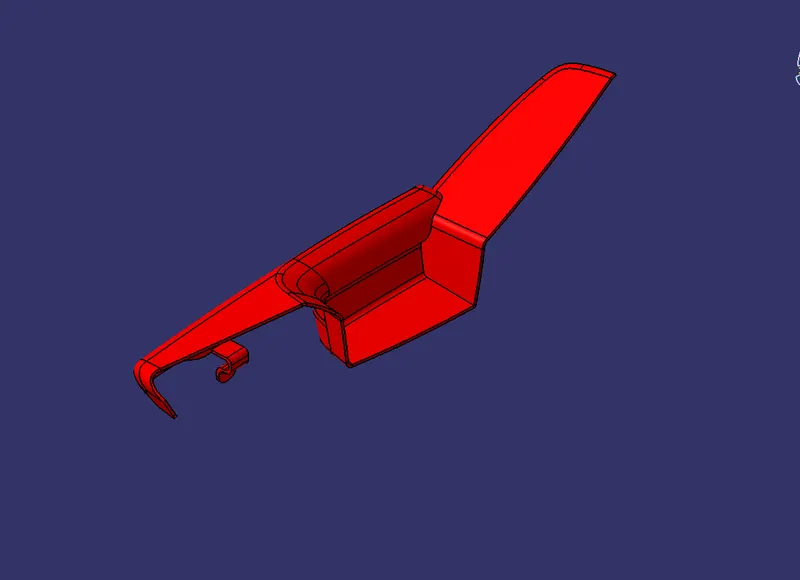
Isometric view:
Front view:
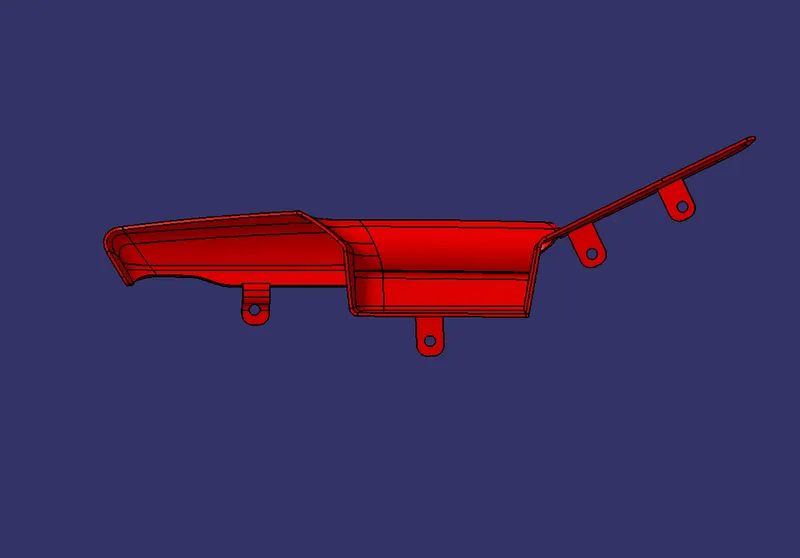
Top view:
Side view:
2.Map Pocket:
Map pockets can be created integrally within the door trim panel by forming a projection region outwardly towards the passenger compartment and then providing a separate panel attached to the rear outboard surface of the trim panel. This type of map pocket protrudes into the passenger compartment. Another type of map pocket such as a recessed map pocket can also be formed within the door assembly such that the storage compartment of the map pocket is generally located between the trim panel and the outer metal panel of the vehicle door. An aperture in the door trim panel defines the opening into the map pocket. Generally, these types of map pockets are formed by a separate map pocket assembly which is fastened to the rear surface of the trim panel. The map pocket assembly includes a front portion and a separate rear portion which are connected together to form the map pocket assembly and define the storage compartment. The rear portion defines a rear wall of the map pocket assembly. The front portion defines a lower front wall and a pair of side walls. The region above the lower front wall is generally open to provide access to the storage compartment of the map pocket. The map pocket assembly is then attached to the rear surface of the door trim panel such that the opening of the map pocket is generally aligned with an opening formed in the door trim panel.
Tooling axis:
Draft Analysis of Map Pocket:
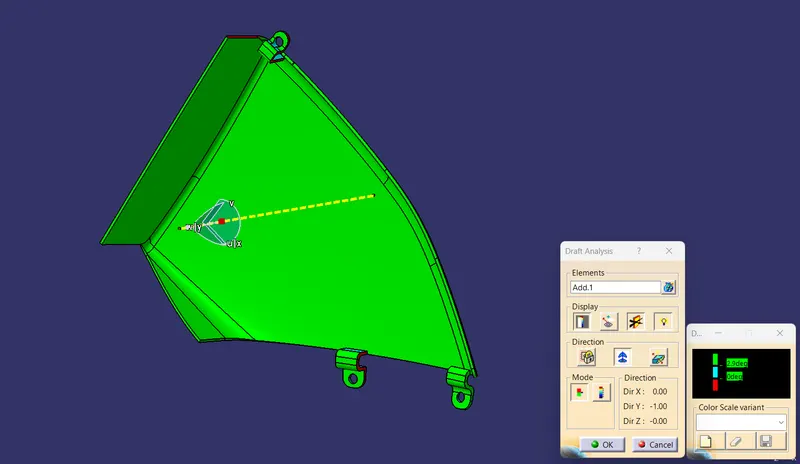
Views:
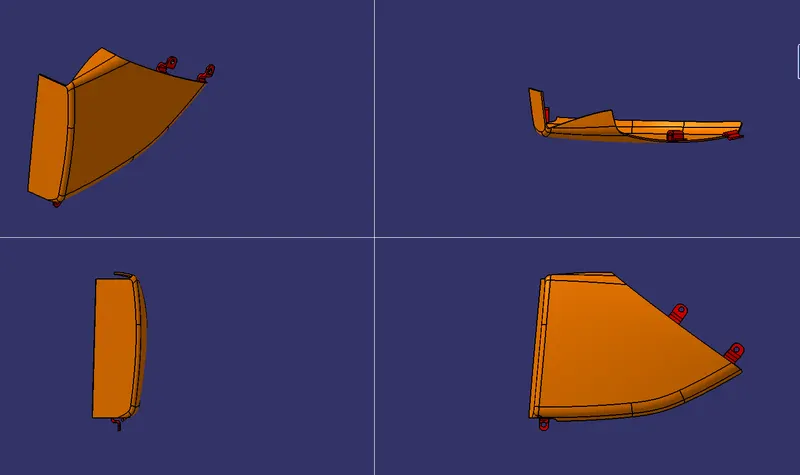
Isometric view:
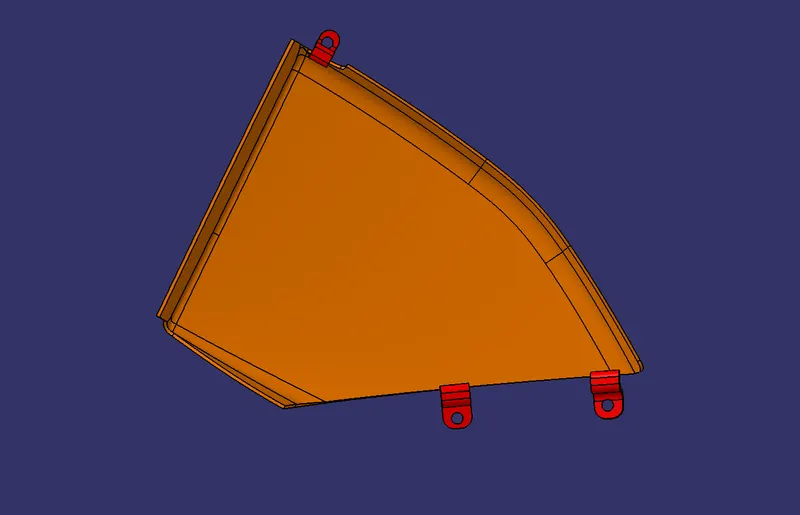
Top view:
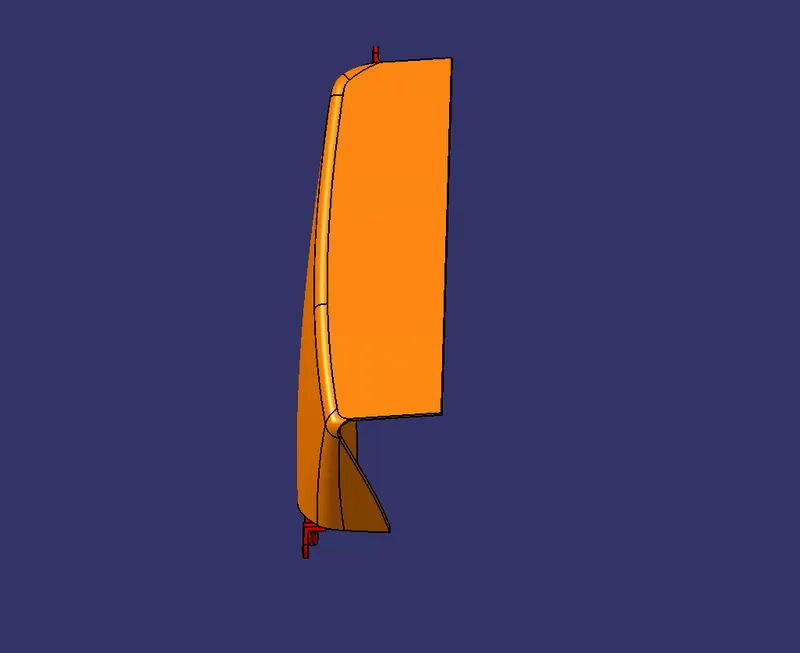
Side view:
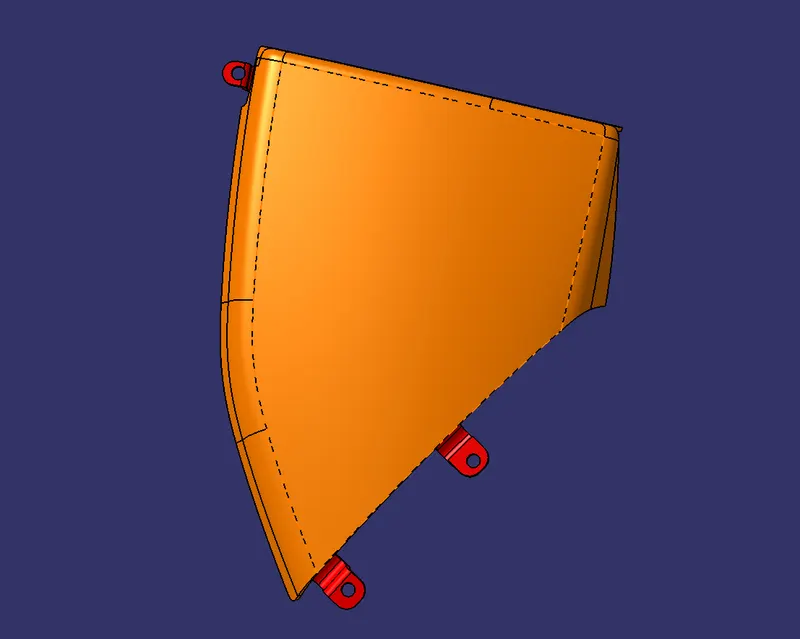
Bottle holder:
-
Introduction: The purpose of this report is to provide an overview of bottle holders in cars, highlighting their convenience and safety features. Car bottle holders have become increasingly popular in modern vehicles, allowing drivers and passengers to securely store beverages while on the move. This report examines the various types, benefits, and considerations associated with car bottle holders.
-
Types of Car Bottle Holders:
Car bottle holders come in different designs and locations within the vehicle. Some common types include:
a. Door-mounted holders: These are typically integrated into the side panels of car doors, providing easy access for both the driver and passengers.
b. Center console holders: Positioned in the central area between the front seats, these holders offer convenient access to beverages for both the driver and the front passenger.
c. Seatback holders: These holders are often found on the backside of front seats, primarily designed for rear-seat passengers to store their bottles.
d. Foldable cup holders: Some vehicles feature cup holders that can be folded out when needed and neatly tucked away when not in use, optimizing space efficiency.
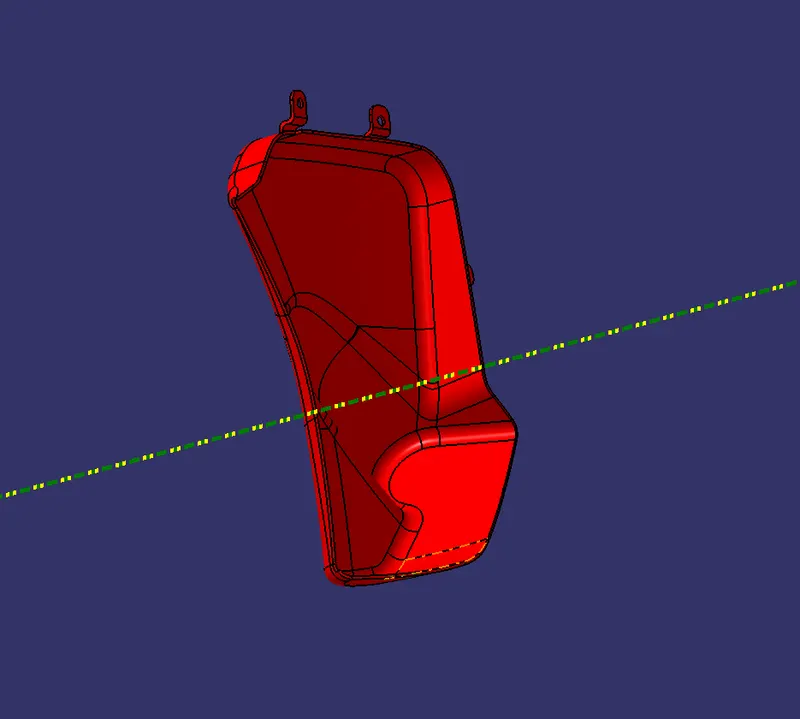
Tooling Axis:
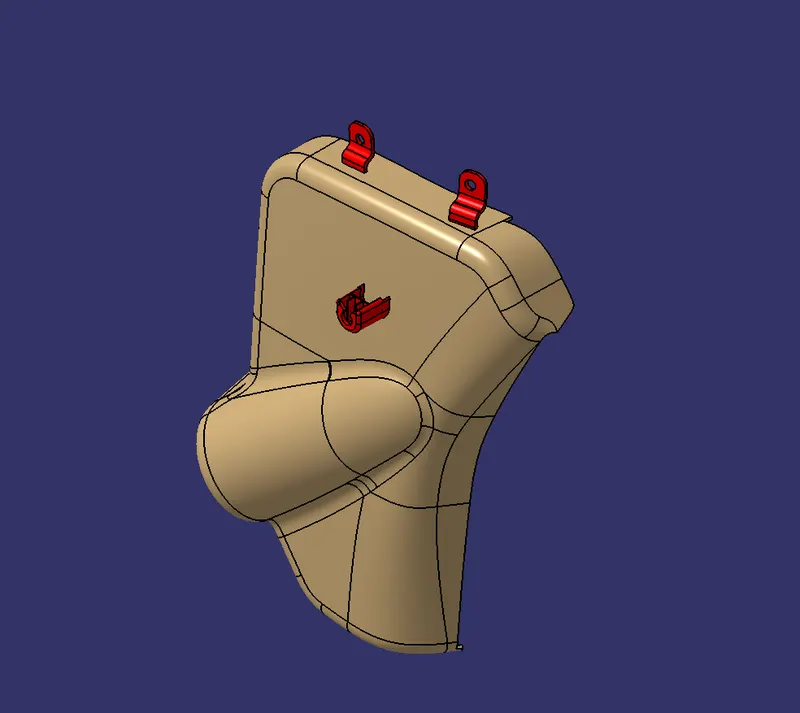
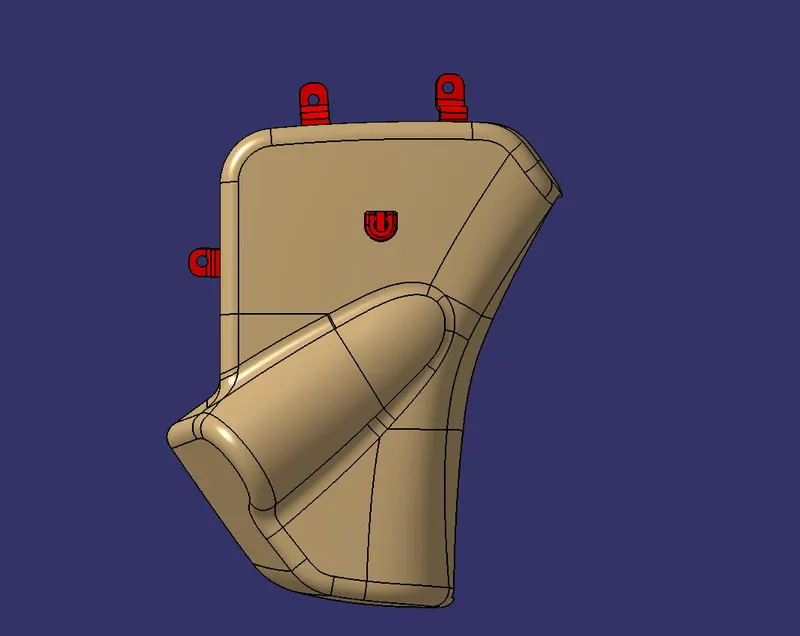
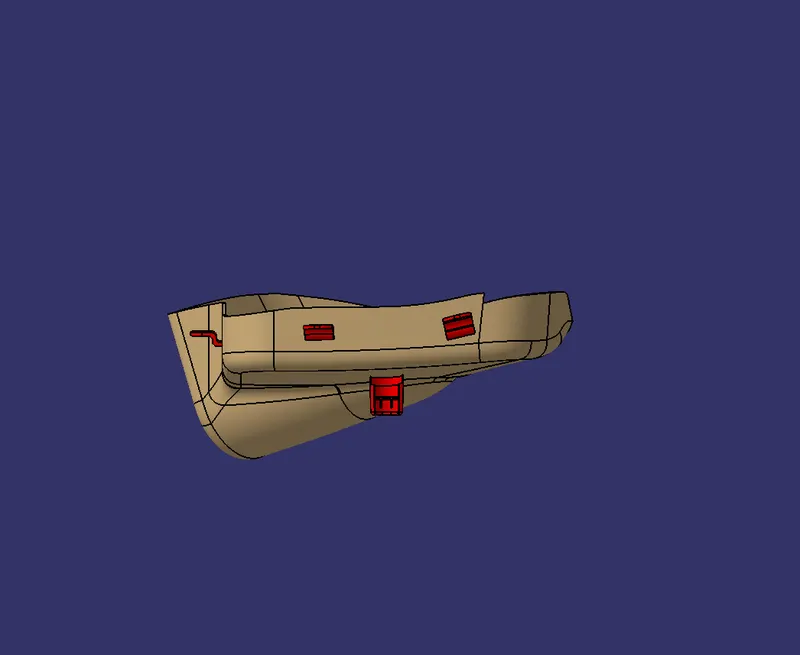
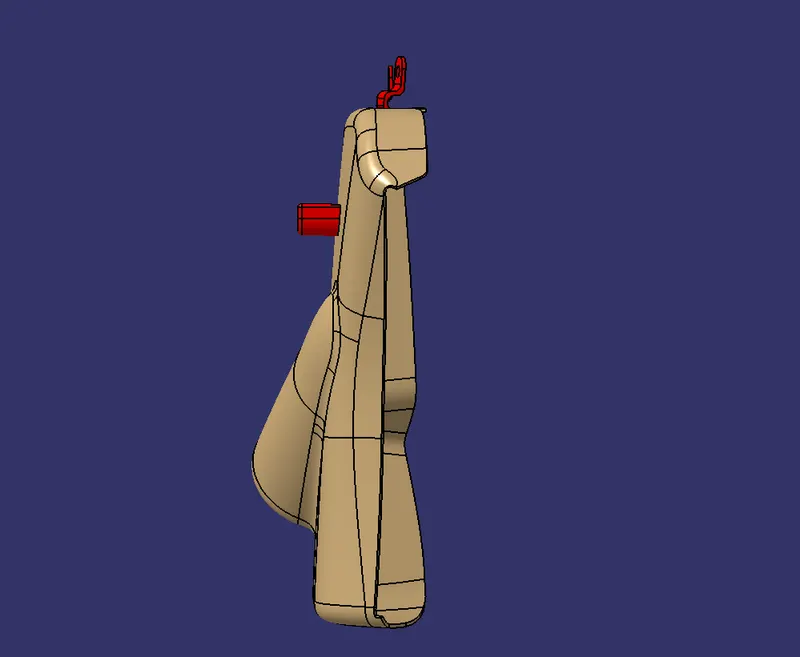
Drafting Analysis:
Views:
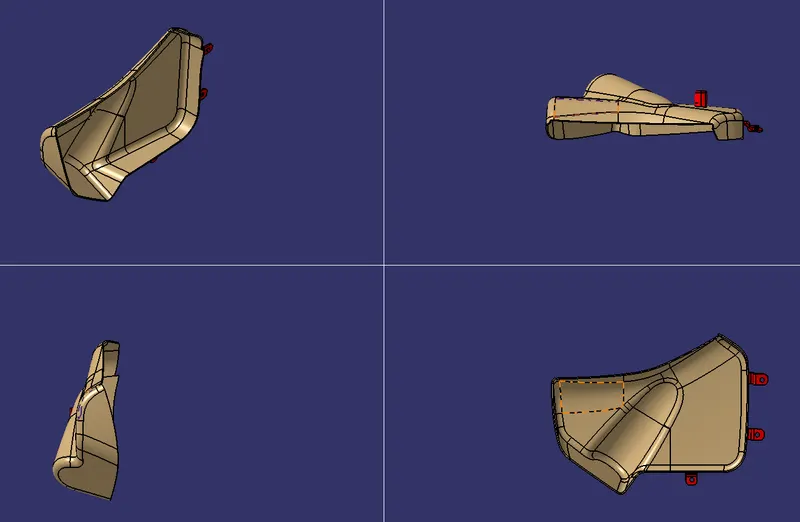
isometric View:
Front View:
Top View:
Side View:
Lower Substitute Door Panel:
The purpose of this report is to provide an overview of the lower substitute door panel, its features, benefits, and potential applications. The lower substitute door panel is a product designed to replace the existing lower portion of a door panel in various settings, such as residential, commercial, and automotive environments. The lower substitute door panel is a customizable component that serves as a replacement for the lower section of a door. It is typically made from durable materials such as wood, plastic, or metal, and is designed to seamlessly integrate with the existing upper portion of the door panel. Aesthetic Appeal: The lower substitute door panel offers an opportunity to update and enhance the appearance of a door, providing a fresh and modern look to the overall design.
The lower substitute door panel offers a practical and visually appealing solution for repairing damaged lower door sections and updating the look of existing doors. With its customizable features, versatility, and potential energy-saving benefits, it provides an attractive alternative to complete door replacement. By considering the specific requirements and preferences, individuals can choose a substitute panel that best suits their needs and enhances the overall aesthetics of their space.
Tooling Axis:
In CATIA, the tooling axis is an essential parameter when working with surface design. The tooling axis defines the direction in which a tool, such as a milling cutter or a trimming tool, will move when interacting with a surface. It is used to control the orientation and movement of the tool during operations like machining or trimming.
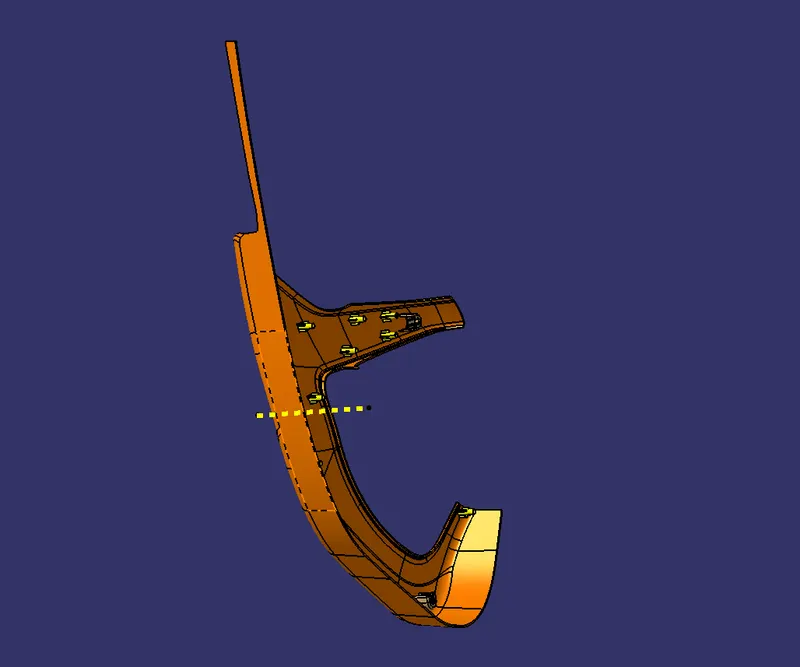
Drafting Analysis:
Views:
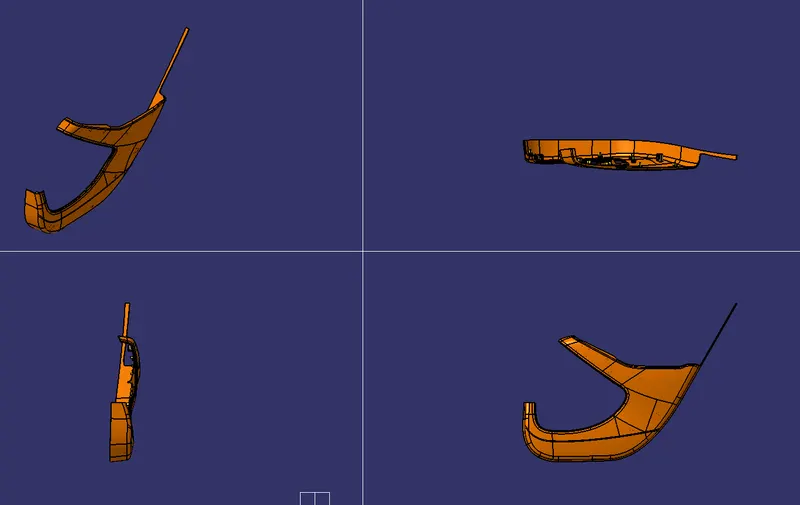
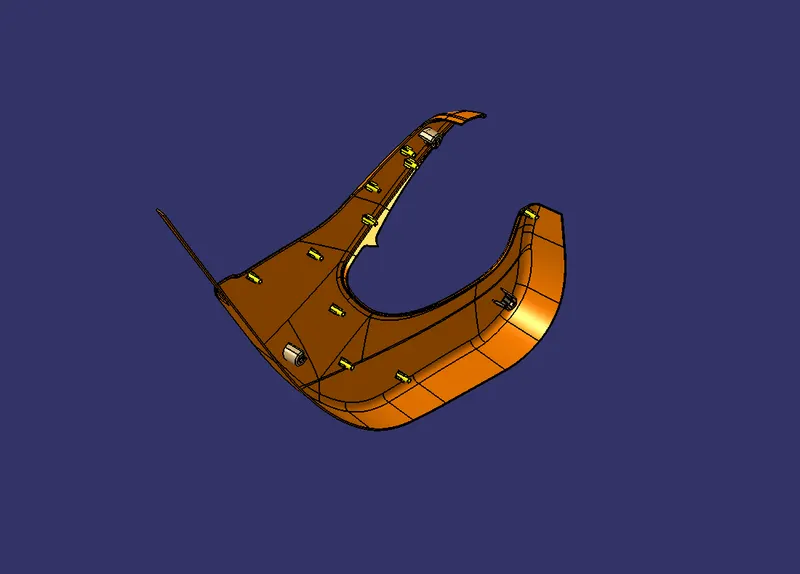
Isometric View:
Front View:
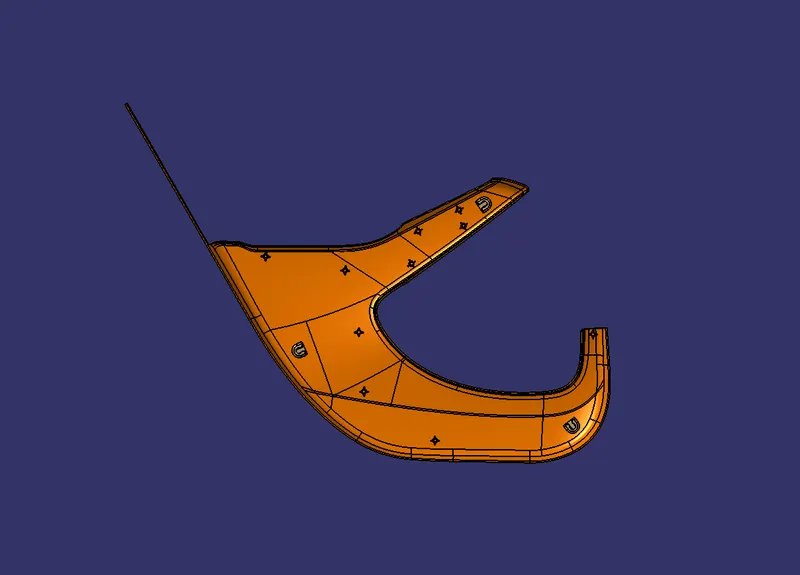
Side View:
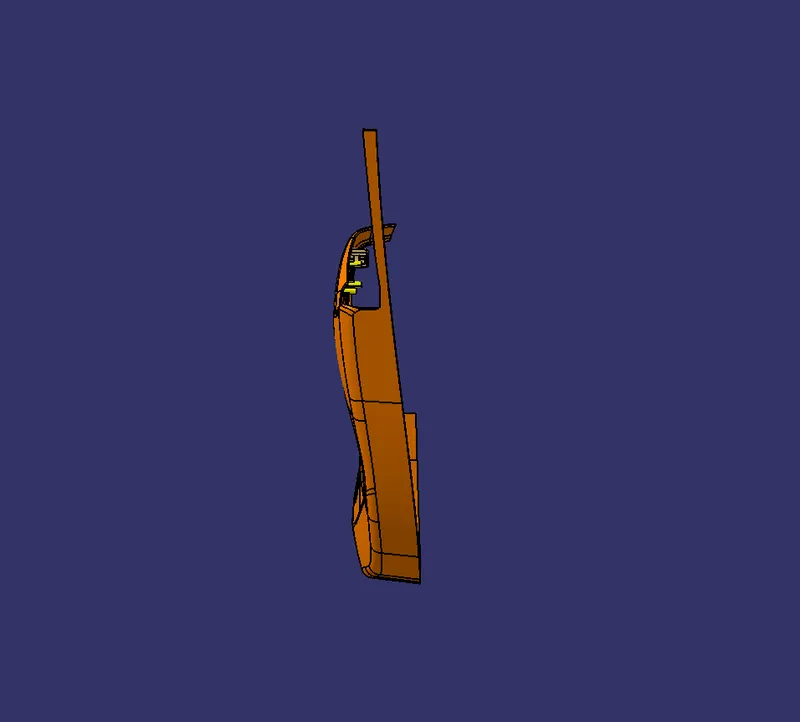
Top View:
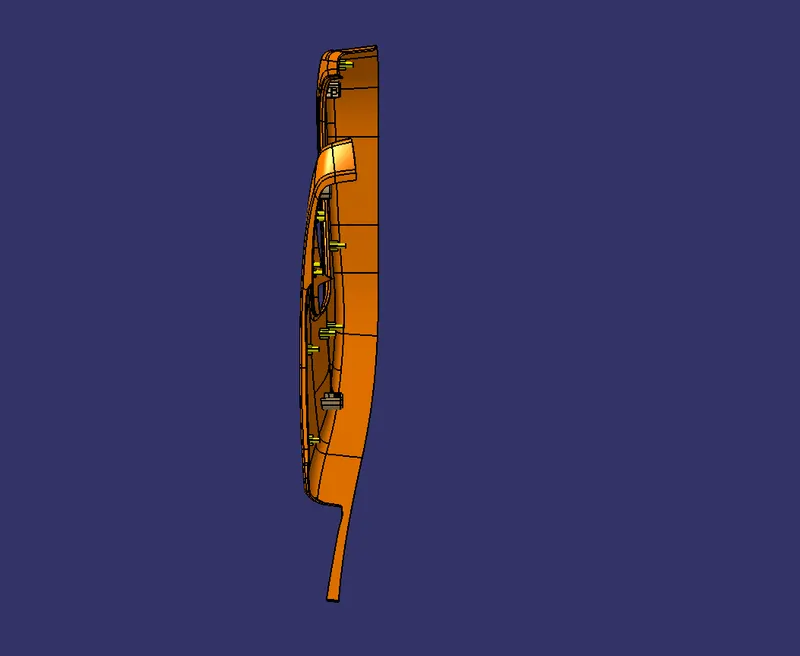
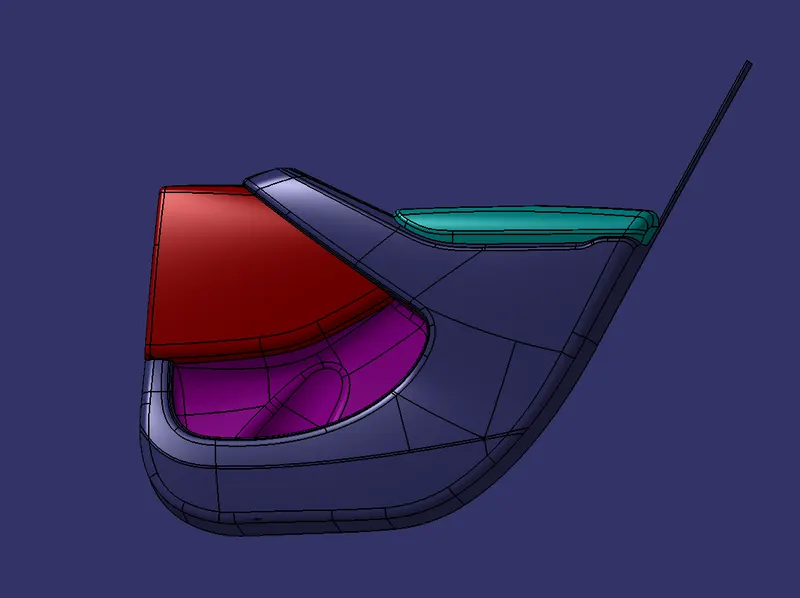
Door Trim Panel:
The design of the car door trim panel should prioritize user comfort and ease of use. Considerations such as armrest height, placement of window and door controls, and storage compartments should be taken into account to enhance the user experience.
The door trim panel plays a crucial role in the overall interior aesthetics of the vehicle. It should align with the vehicle's design language and harmonize with other interior elements in terms of color, texture, and material selection.
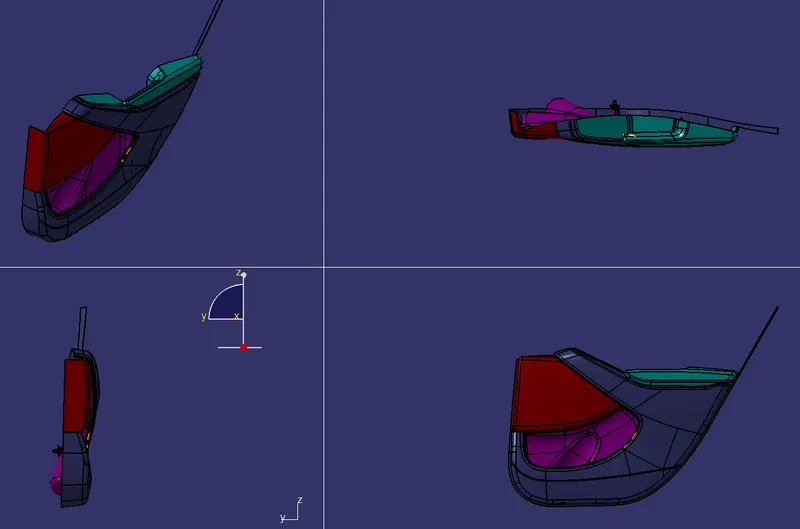
The design of the trim panel should consider the integration of various components such as speakers, switches, handles, and airbags. Proper placement and integration of these elements ensure functionality and safety.
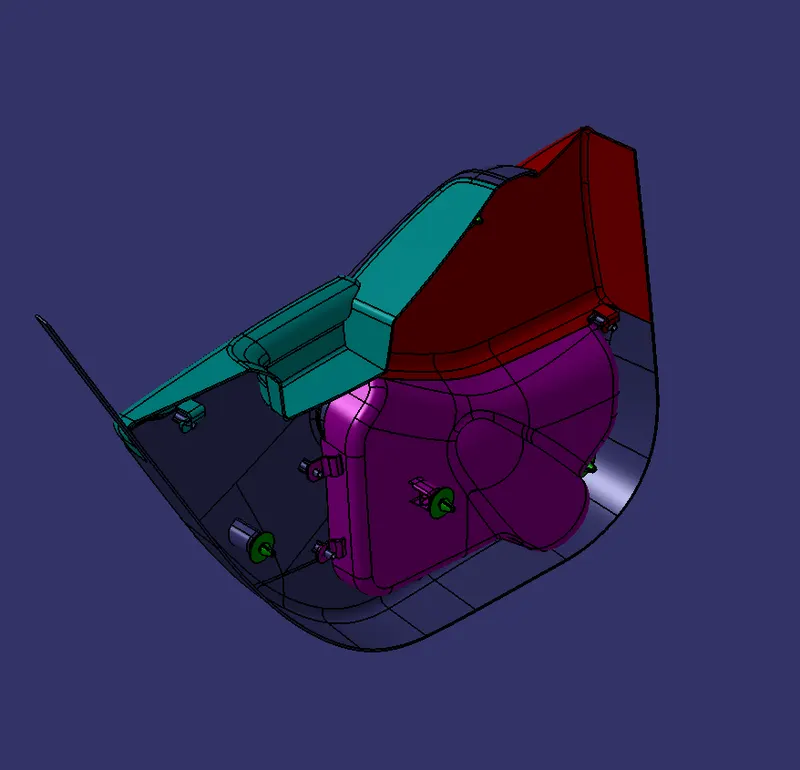
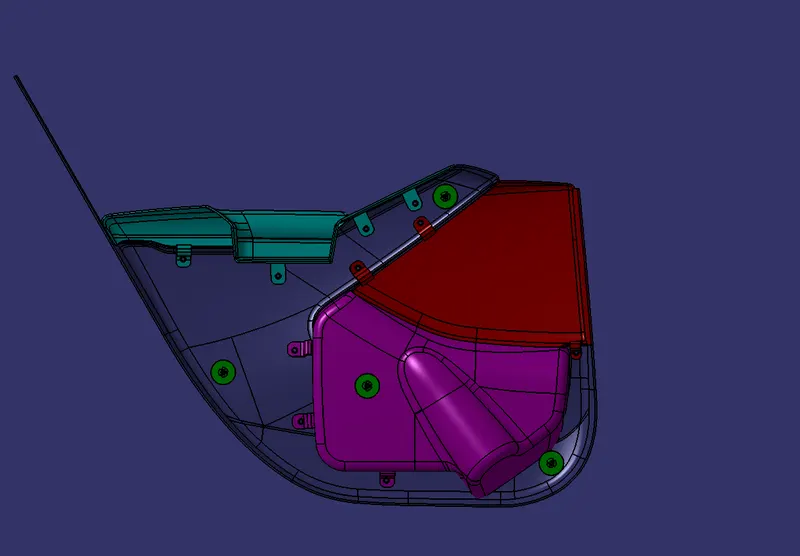
Final Outpu:
Conclusion:
The design of car door trim panels is a critical aspect of interior vehicle design. It involves considerations of aesthetics, ergonomics, material selection, and integration with various components. By prioritizing user comfort, functionality, and visual appeal, car door trim panels contribute to an enhanced driving experience and a well-designed interior. Manufacturers should also focus on efficient manufacturing processes and environmental sustainability to meet industry standards and customer expectations.