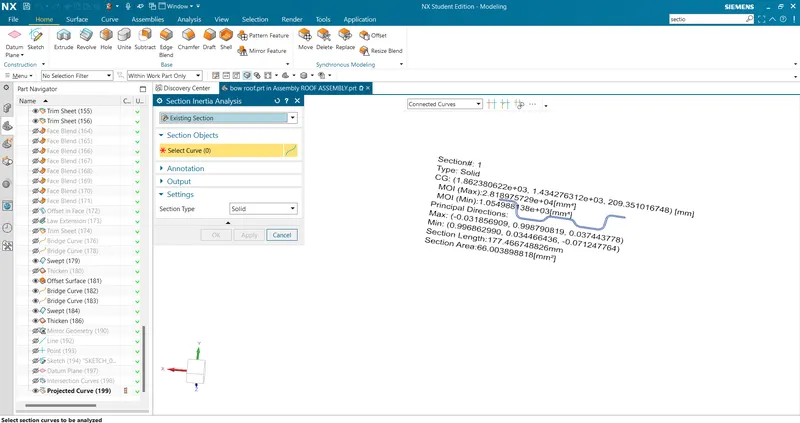
Roof challenge
| section | ALPHA | t | s | Rx | Ry | ly | Qr | ok/not ok |
| 1 | 1.06 | 0.75 | 522.95 | 6136.91 | 3178.35 | 6.675e+03 | 31.44 | ok |
| 2 | 1.27 | 0.75 | 489.25 | 5442.104 | 7362.53 | 4.247e+03 | 93.49 | ok |
| 3 | 0.79 | 0.75 | 450.8 | 3271.58 | 15529.78 | 1.85e+03 | 3.306 | ok |
| 4 | 0.26 | 0.75 | 149.85 | 5517.89 | 5228.58 | 1.054e+03 | 51.51 | ok |
snow load condition
| section | L | R | t | l | W | ok/not ok |
| 1 | 1964.3 | 4052.59 | 0.75 | 811.8 | 2.007 | ok |
| 2 | 1964.3 | 5727.55 | 0.75 | 296.7 | 1.845 | ok |
| 3 | 1964.3 | 5708.180 | 0.75 | 519.7 | 2.084 | ok |
| 4 | 1964.3 | 5225.32 | 0.75 | 106.4 | 1.5 |
ok |
heat distortion condition
Curvature study- As the bend in the roof is more in the front side of roof, the bending resistance is more in thefront and the bow roof 1 can hence be placed closer to the centre roof rail.
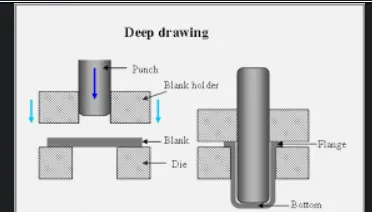
Manufacturing processes used- 1) Deep drawing- Deep drawing is a process in which sheet metal is radially drawn in a forming die by mechanical action of punch. It is thus a shape transformation process with material retention. The process is considered deep drawing when the depth of the drawn part exceeds its diameter.
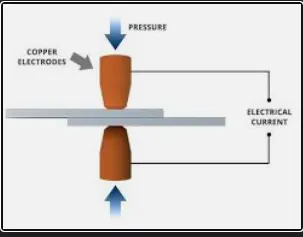
2) spot welding- It is a type of electric resistance welding used to weld various sheet metal products through a process in which contacting metal surface points are joined by heat obtained from resistance to electric current.
ROOF PARTS- FRONT ROOF RAIL-
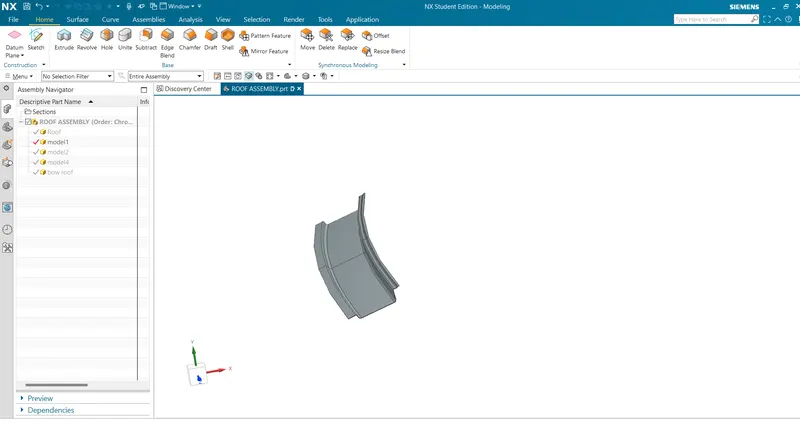
REAR ROOF RAIL-
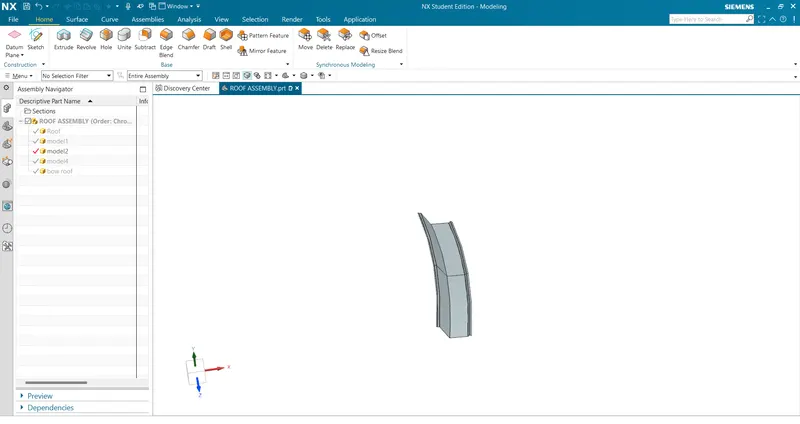
CENTRE ROOF RAIL-
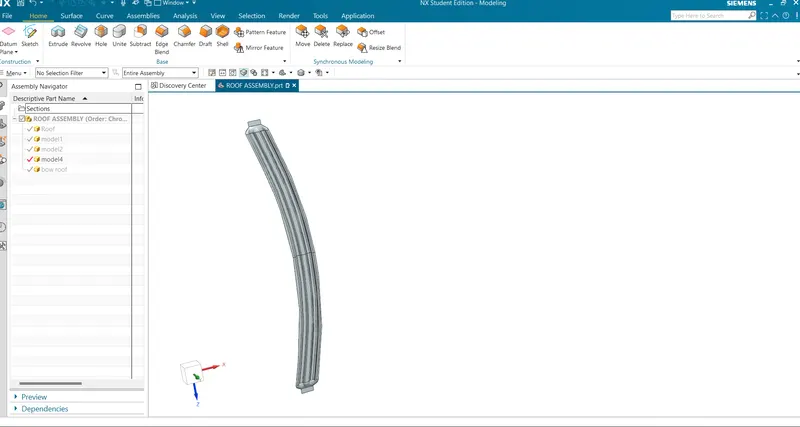
BOW ROOF -
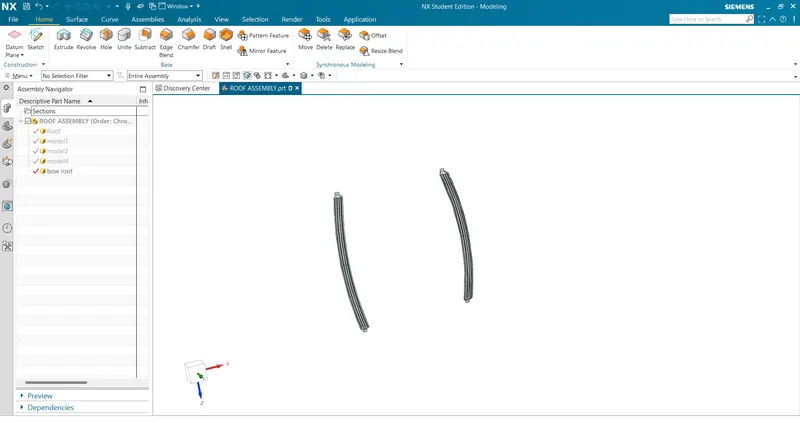
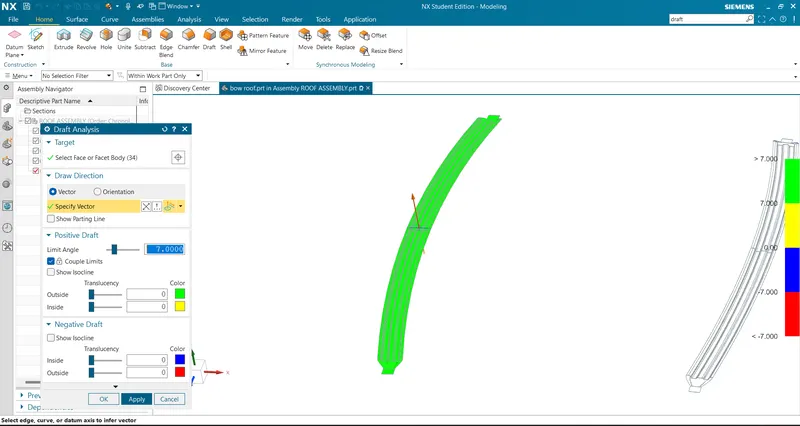
DRAFT ANALYSIS-
FRONT ROOF RAIL-
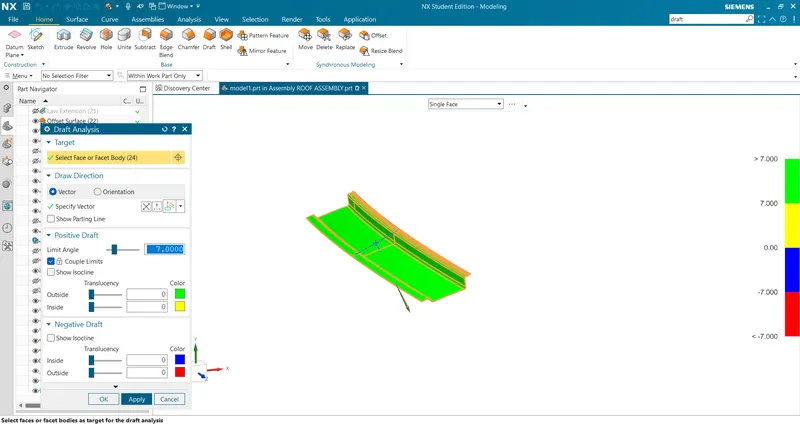
REAR ROOF RAIL-
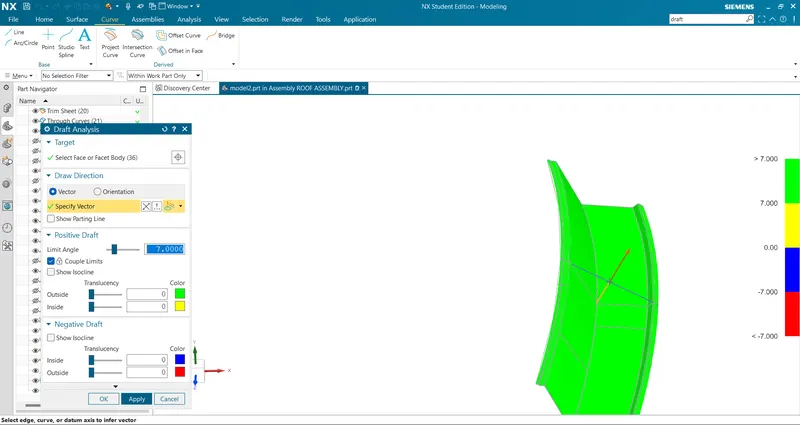
CENTRE ROOF RAIL-
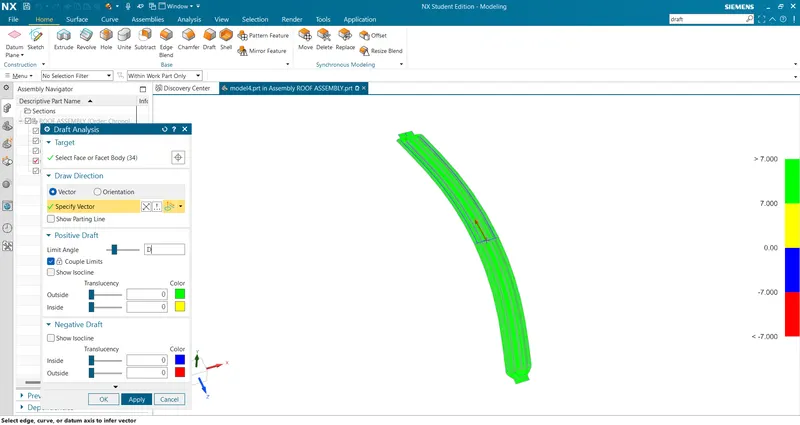
BOW ROOF-
Section Modulus -
Front roof rail-
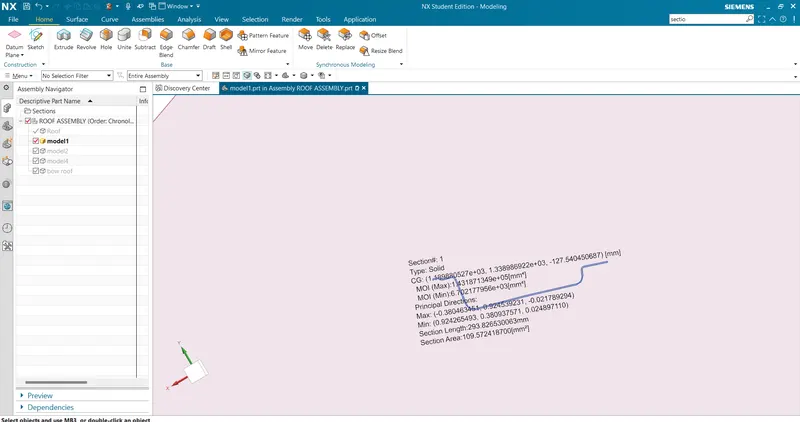
REAR ROOF RAIL-
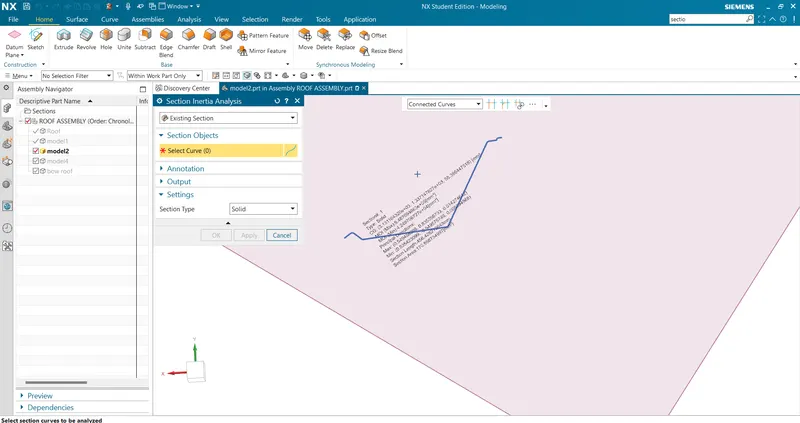
CENTRE ROOF RAIL-
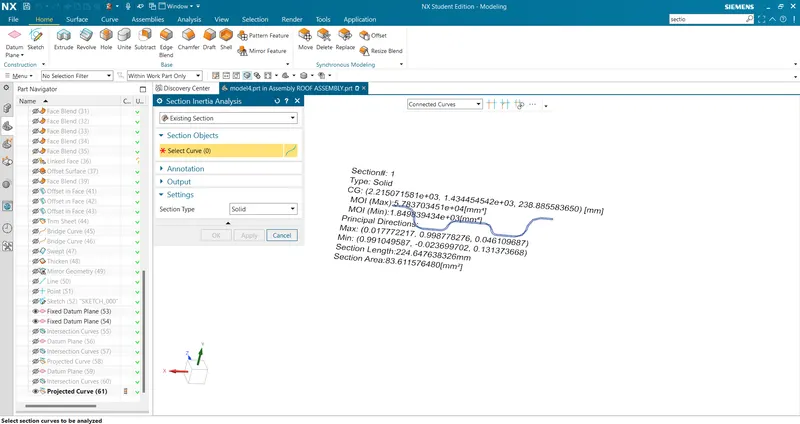
BOW ROOF-