Hood design-Week 2
HOOD DESIGN
The hood or bonnet is the HINGED cover over the engine of motor vehical. Hoods can open to allow access to the engine compartment, or trunk (boot in on rear-engine and some mid-engine vehicles) for maintenance and repair.
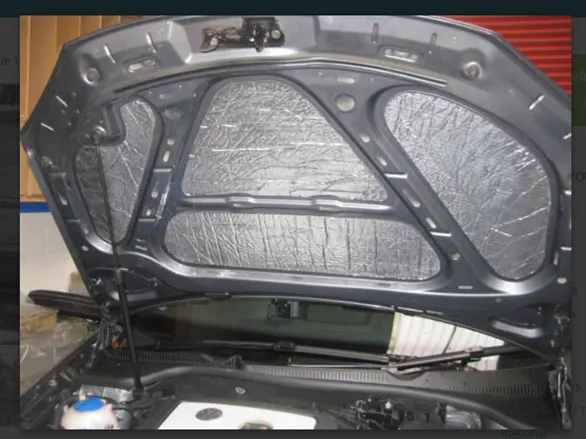
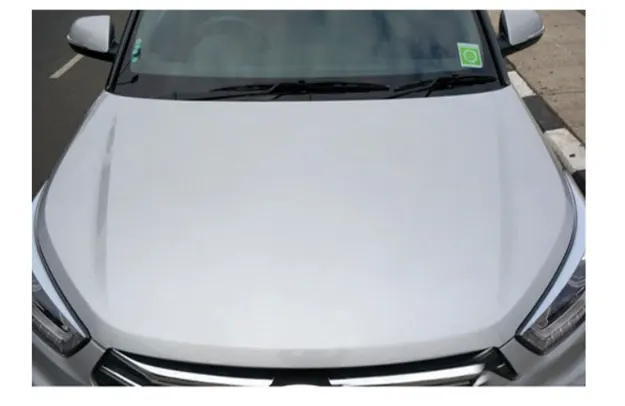
The HOOD is an opening body panel that covers the engine in a front engine vehicle. The hood is also considered as another type of door in a vehicle as it consists of an outer panel and inner panel. The inner panel provides strength while the outer panel functions as the metal cover.
PARTS OF AN HOOD:
Basically, the hood has the inner panel, outer panel, and reinforcement (it will provide the strength) and emboss. Latch and striker mechanism is used to open and close the hood whenever is needed. Latch and hinge is needed some reinforcement for strength.
TYPES OF HOOD SUPPORT:
There are two types of support is there.
- Gas stay
2.Support rod
GAS STAY
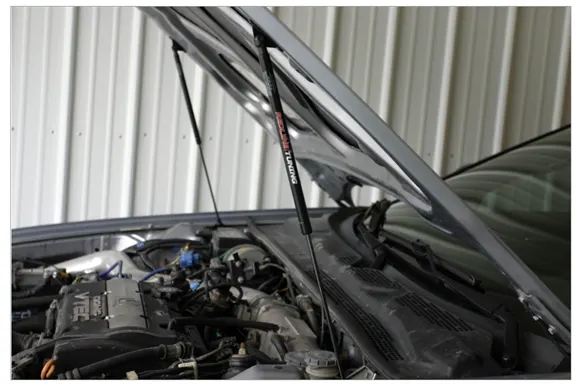
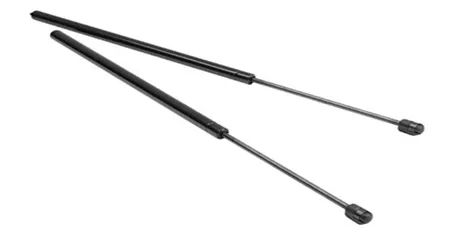
A gas spring is a type of spring that, unlike a typical mechanical spring that relies on elastic deformation, uses compressed gas contained within an enclosed cylinder sealed by a sliding piston to pneumatically store potential energy and withstand external force applied parallel to the direction of the piston shaft.
SUPPORT ROD
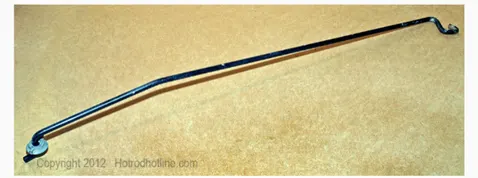
Support rod is basically long cylindrical rod. It safely keeps an engine hood in an open state even if external forces are abruptly generated due to vibration & wind. This is widely used in many cars, because this very easy and cheap, in this type we have to lift the hood by own and place the support rod in the space provide either in the hood of engine compartment. This is mostly used for where the car bonnet weight is small.
PEDESTRIAN SAFETY:
For pedestrian safety, global NCAP (New Car Assessment Program) has the principles which use in crash tests with a pedestrian.
When designing the hood, we should consider those principles and allow our design to get qualified with good results from the NCAP which impact in the sales of the vehicles.
PEDESTRIAN PROTECTION TEST PROCEDURES:
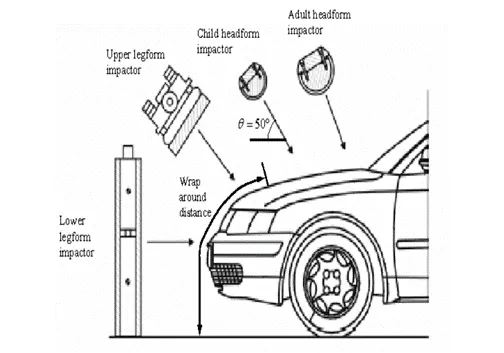
In this test, the hood is divided into the child impact zone and the adult impact zone. From the results, the grade and rating will be to the vehicle.
We should consider both the child head impact and the adult head impact.
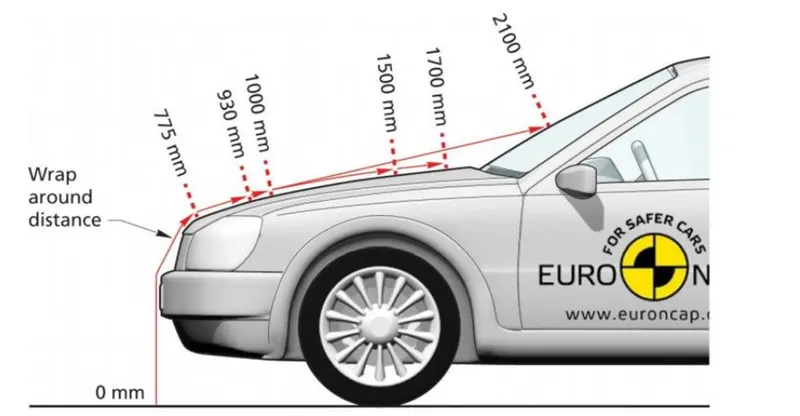
- Wrap around distance: It is the process of tracing the points on the front outer structure. It includes, but not limited to the hood wings, wind-screen scuttle, and wiper-arms, windscreen frame. It is bounded by the geometric trace of the 1000mm wrap around the line in the front, bonnet side reference lines, and 2100mm wrap around the distance.
- SIDE REFERENCE LINE: It is defined as the geometric trace of the highest points of contact b/w a straight edge of 700mm long and the side of the bonnet. When a straight edge held parallel to the lateral vertical plane of the car and inclined inwards by 45 degree is traversed down the side of the bonnet top and A-pillar.
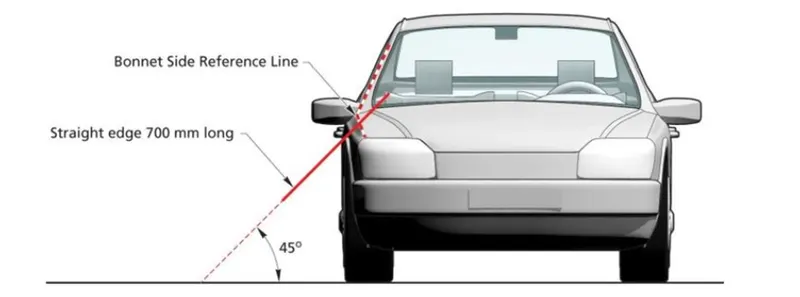
The side reference line allows checking the impact trace by a pedestrian.
- If the side reference line falls on the fender, the WAD will be greater and the impact zone will be less.
- If the side reference line falls on the hood the WAD will be lesser and the impact zone will be high.
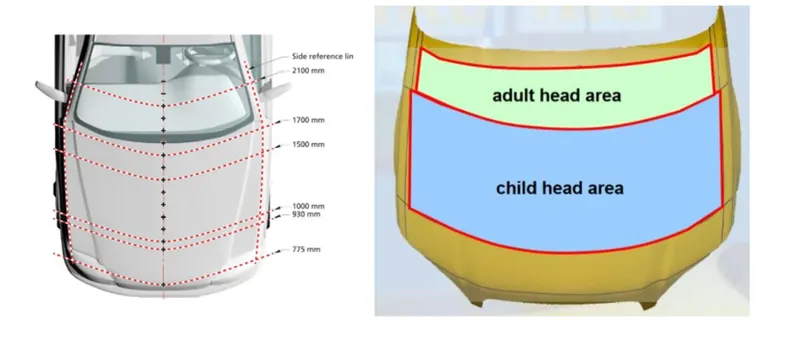
As per NCAP, the child head impact zone lies in b/w 1000WAD-1500WAD, and the adult head impact zone lies in between 1500WAD-2100WAD.
MATERIAL SELECTION:
- Hood is made out of steel or aluminium, if the car body required less weight ratio carbon fiber or dry carbon is also used.
- Silicon polymer and silicon copper paste for mastic seal.
- Reinforcement vinyl ester composite for latch.
- Steel for hinges.
AIM:
To design the car hood and understand the mechanism behind the design of hood, then development & its safety features as per the design consideration.
The following task is performed:
- Design outer panel with the hem.
- Develop the inner panel.
- Develop all the necessary reinforcements.
- Mirror and position the hinge & striker.
- Provide mastic data
- Provide the required emboss definition.
- Develop a detailed report for the mastic position and emboss you have placed.
MASTER SKETCH
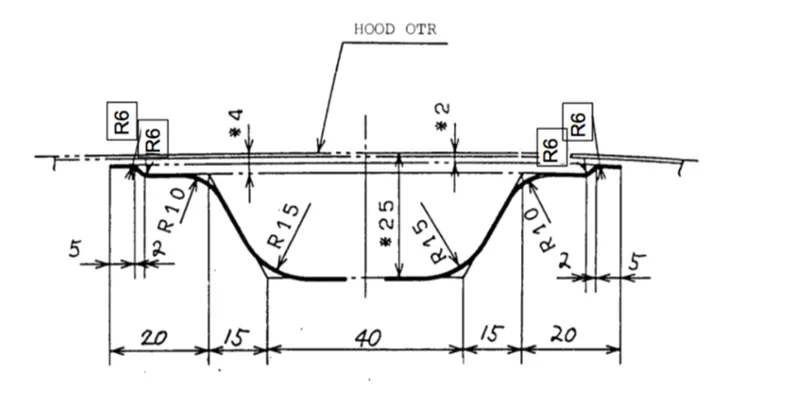
Data to be used:
Hood thickness information.
- Outer panel thickness = 0.75mm
- Inner panel thickness = 0.75mm
- Reinforcement thickness = 1.5mm
The process involved in designing hood as a sheet metal operation is
- Blanking
- Hemming
- Deep drawing
- Embossing
DESIGN OF HOOD
Inner panel design
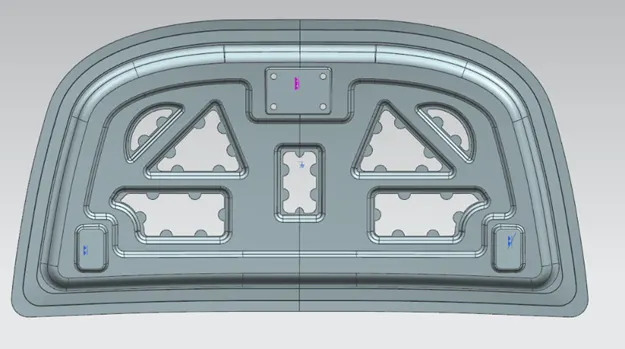
- The hood inner panel is required to have a high initial reaction force against the impact excreted on the hood to enhance the energy absorption capacity. The hood is further required to minimize a reduction of a reaction force by deformation in a collision.
- It is an object of the present invention to provide hood inner panel capable of reduction of a reaction force of the hood inner panel even if a level of deformation of a hood of a vehicle increase, and ensuring a sufficient energy absorption capacity.
- In the inner panel only, we can research and implement the safety of pedestrians and as well as the driver in this panel only we can attach the reinforcement, emboss, mastic points, etc.
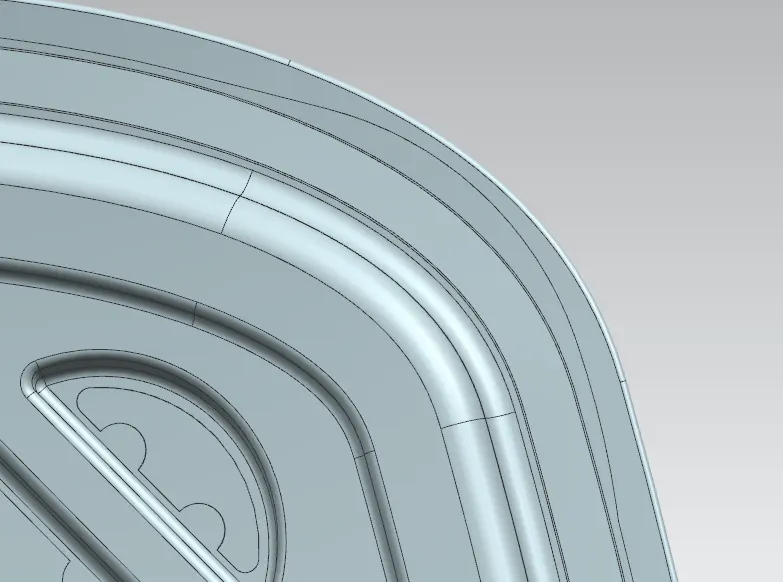
Embossing in sheet metals
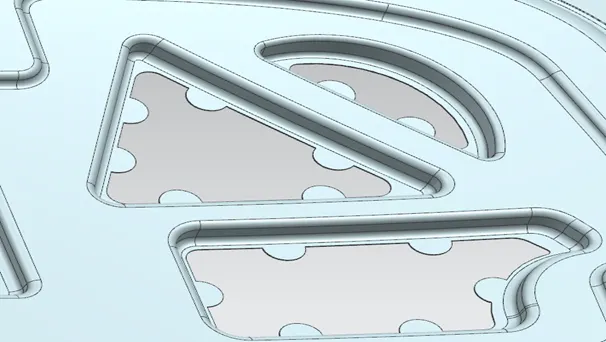
- Sheet metal embossing is a stamping process for producing raised or sunken designs or relief in sheet metal. This process can be made by means of matched male and female roller dies, or by passing sheet or a strip of metal between rolls of the desired pattern.
- The metal sheet embossing operation is commonly accomplished with a combination of heat and pressure on the sheet metal, depending on what type of embossing is required. Theoretically, with any of these procedures, the metal thickness is changed in its composition.
- A metal sheet is drawn through the male and female roller dies, producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet. The pressure and a combination of heat actually “irons” while raising the level of the image higher than the substrate to make it smooth. The term “impressing” refers to an image lowered into the surface of a material, in distinction to an image raised out of the surface of a material.
DEEP DRAWING
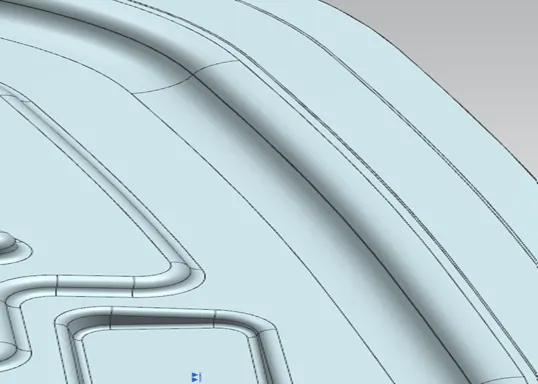
- Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. ... The process is considered "deep" drawing when the depth of the drawn part exceeds its diameter. This is achieved by redrawing the part through a series of dies.
- Deep drawing is a manufacturing process that is used extensively in the forming of sheet into a cup or box-like structure pots and pans for cooking, containers, sinks, automobile parts, such as panels and gas tanks, are among a few of the items manufactured by sheet metal deep drawing.
- A deep drawing of sheet metal is performed with a punch and die. The punch is the desired shape of the base of the part. Once drawn. The die cavity matches the punch and is a little wider to allow for its passage, as well as clearance. The sheet metal thickness is assumed to remain constant. However, there are changes in thickness in certain areas, due to the forces involved.
HEMMING IN SHEET METALS
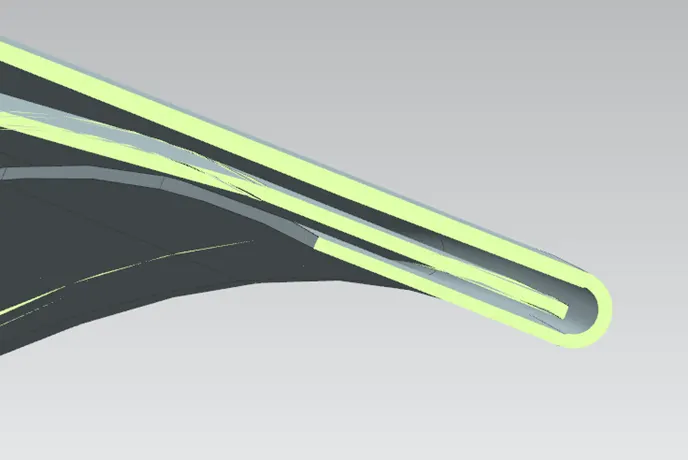
- Hemming is sheet metal forming process in which sheets are joins by bending it usually to 1800 automotive body panels and automotive parts such as deck-tide. Trunk-lids, doors, hoods, and tailgate are formed by hemming processes.
- Conventional die hemming is suitable for mass production. In die hemming, the flange is folded over entire length with a hemming tool. Normally the actual hemming is a result of a forming operation in which the flange is formed with a hemming tool after the drawing and trimming operations have been completed.
- Roll hemming carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps.
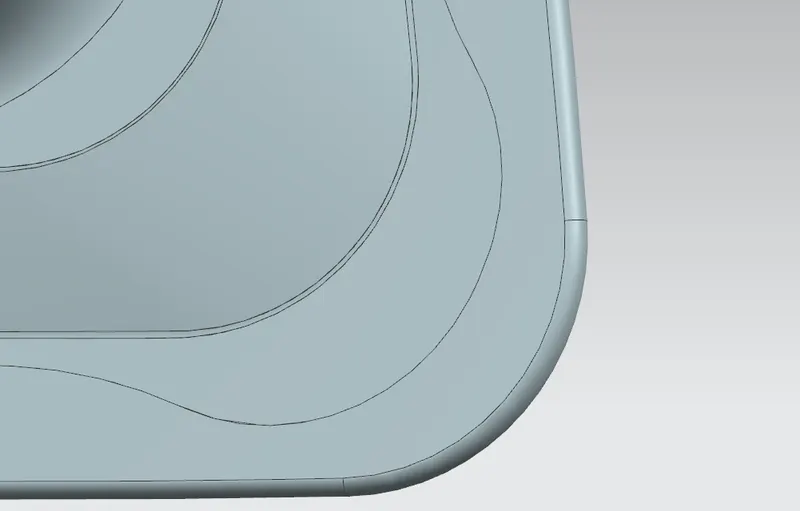
While doing the hemming process, a relief angle is formed as a product of hem when attaining at corner of the sheet metals.
MASTIC DATA
A mastic sealant data is used to fix or combine the hood inner panel. Its influence area is 80mm dia.
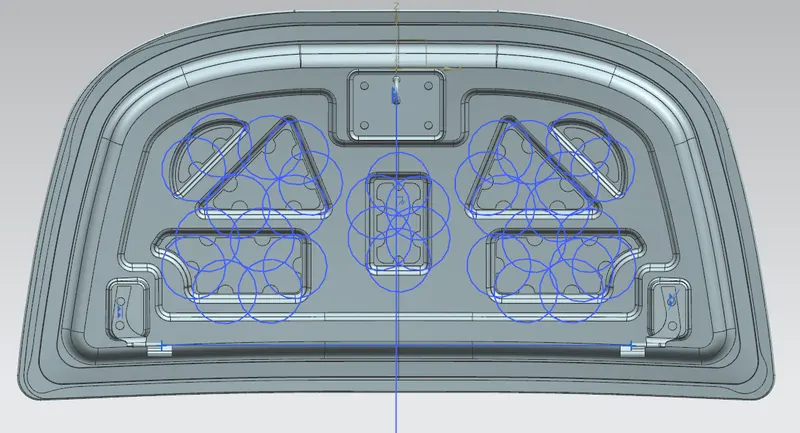
- They can provide thermal and acoustical insulation, and may serve as fire barriers. They can have electrical properties. Sealants can also be used for simple smoothing or filling. They are often called upon to perform several of these function at once.
- A sealant has three basic functions: it fills a gap b/w two or more substrates; it forms a barrier through the physical properties of the sealant itself and by adhesion to the substrate; and it maintain sealing properties for the expected lifetime, service condition, and environments. The sealant performs this function by way of correct formulation to achieved specific application and performance properties.
HOOD COMPONENT
- LATCH
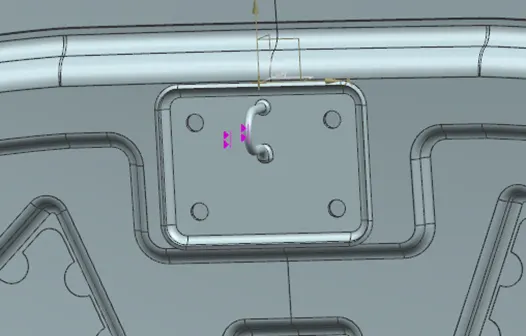
A hood latch is a very simple component. Its basically the fastener that keeps your hood closed shut. This latch ensure that your hood is securely connected to your vehicle and tht it doesn’t pop open unexpectedly
When tension is applied to the cable from the hood release handle, it pivots the secondary latch, which pulls away from a retaining seat located under the hood. By design, the secondary latch then releases the hood a few inches before latch takes over.
- HINGE
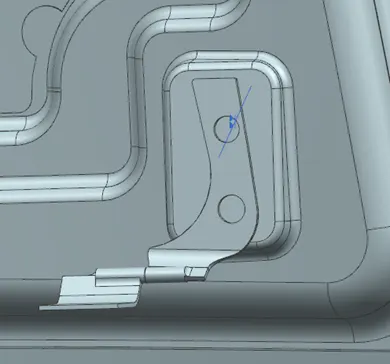
Hinge is a component that fixes the hood to the fenders of the car. The latch must be fixed perpendicular to the hinge axis so that the hood opens or closes properly.
LATCH TRAJECTORY MOTION
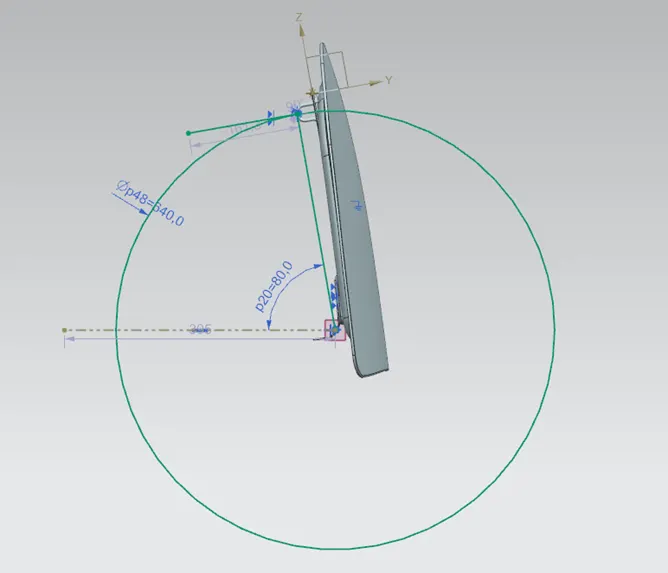
While opening or closing the hood, the latch must be perfectly aligned to the fixing or striker point. For that , the latches trajectory must be perpendicular to the hinge axis.
IMPACT FORCE DISTRIBUTION IN HOOD DESIGN
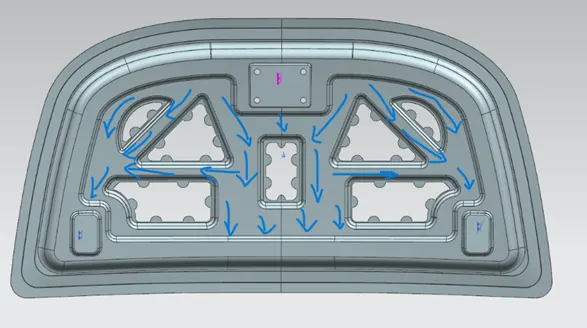
A Hood design must be made in such a way that when a force is impacted in the front of the hood, all the force must be directed outwards from the vehicle. And the distribution of the force must be controlled along with the hood.
HOOD VIEW
HOOD_BACKVIEW
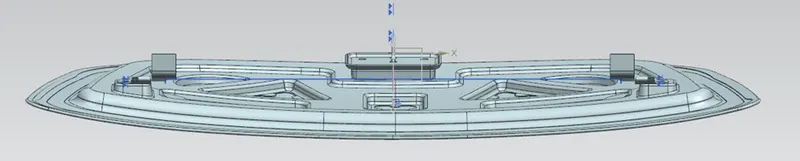
HOOD_LEFT VIEW
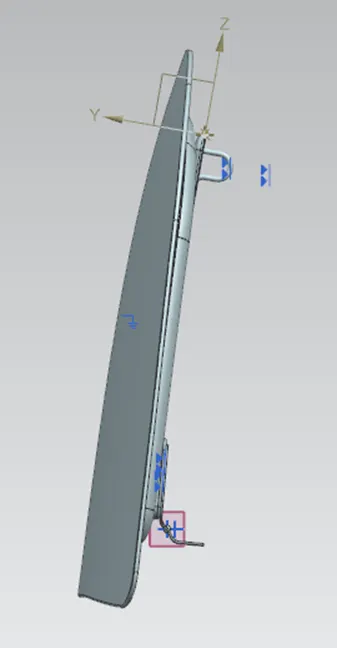
HOOD_ISOVIEW
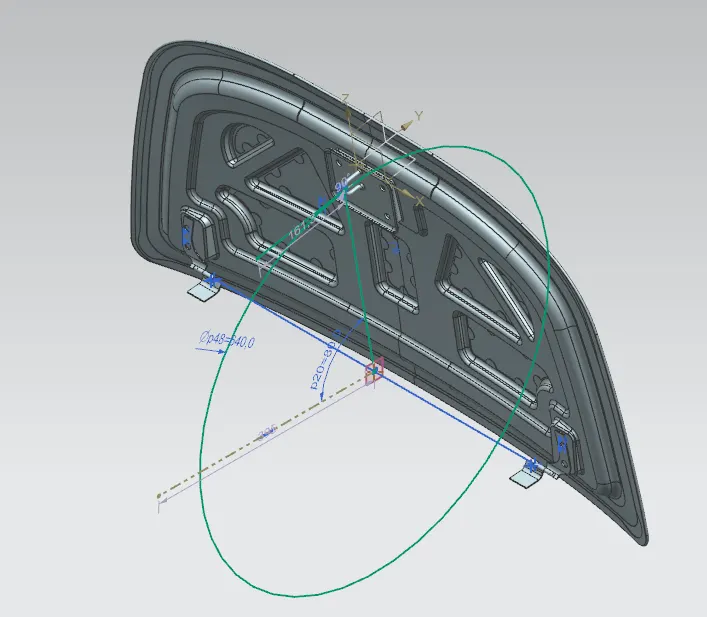
HOOD_RELIFE
Conclusion
Therefore, we have design a hood that falls under the rules and regulations of the manufacturer’s standards.