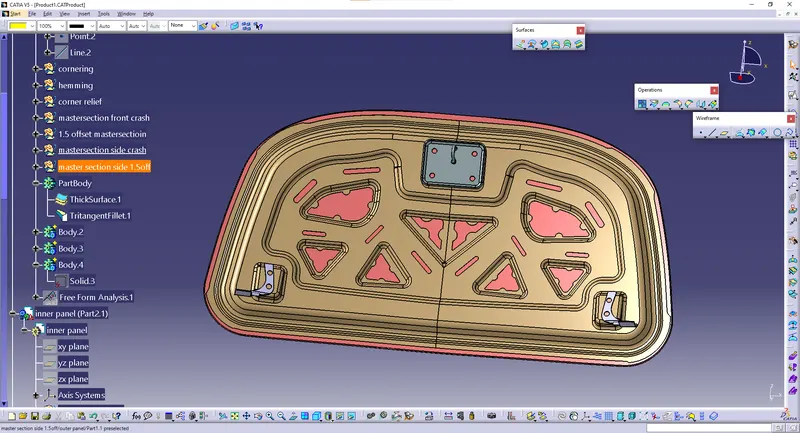
Hood design-Week 2
DESIGN OF HOOD
Aim:
To Design & Assemble Hood outer panel, inner panel and the necessary reinforcements by following the Design parameters & Master section which is given to us as an input.
Introduction:
The project report deals with the explanation of steps and procedure followed while developing the HOOD Assembly of a car using CATIA V5. Using the styling surface and master section as input, we were able to create a HOOD outer panel and inner panel with features like embossments and mastic points. After creating the HOOD outer & inner panels, we have created a complete HOOD assembly consisting of the outer panel, inner panel, latch, hinge & reinforcements. In the end, a Draft Analysis has also been performed using the main tooling axis to check the manufacturability of the components.
Methodology:
- Creating Hood Inner Panel
- Creating Hood Outer Panel
- Creating Embossment for Hinge
- Creating Embossment for Latch
- Creating Reinforcements
- Assembling the components
- Performing Draft Analysis on CAD Model
Hood Thickness Information :
- Outer Panel Thickness = 0.75mm
- Inner Panel Thickness = 0.75mm
- Reinforcement Thickness = 1.5mm
Theory:
HOOD:
The hood or bonnet is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment or trunk on rear-engine and some mid-engine vehicles for maintenance and repair. It generally covers the engine and other essential accessories like battery, Radiator, electrical components, etc. of the car which are exposed outside. The Hood consists of an outer panel and an inner panel. The inner panel provides strength and support, where the outer panel is a metal cover that has styling factors.
HOOD MASTER SECTION :
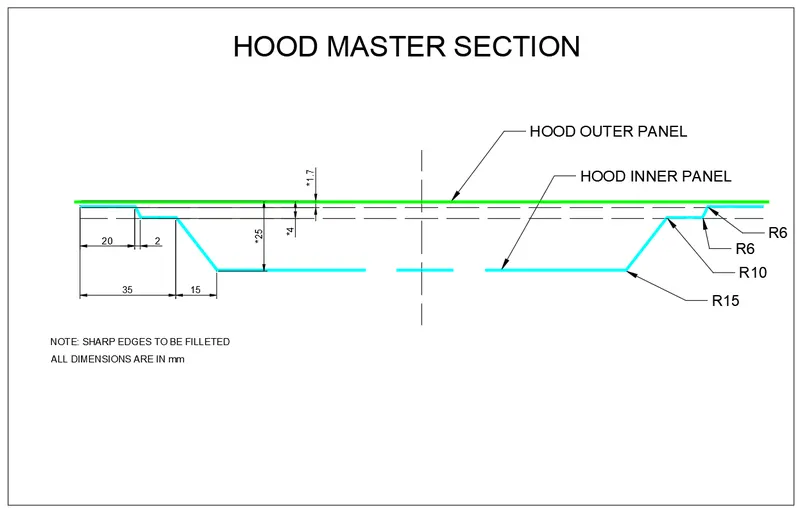
Master section is already provided as per the manufacturing requirements.
Initial design was created from the master section that was already provided. Embossing is a metal forming process for producing raised or sunken designs or relief in sheet material by means of matched male and female roller dies, theoretically with no change in metal thickness. Embosses are created to provide additional strength and to direct the forces from the front collision towards the hinge of the car.
Hood outer panel:
Outer panels are the aesthetic elements of a car. It is the styling team who provides the skin for the outer panel. The shape, position and size of the hood should satisfy the safety norms. So while designing the hood we should give more importance to pedestrian safety. The outer panel is attached to the inner panel by hemming. So, it is necessary to provide required hemming flange and reliefs for the hemming operation. We also provide mastic sealants between the outer panel and the inner panel to reduce the vibration.
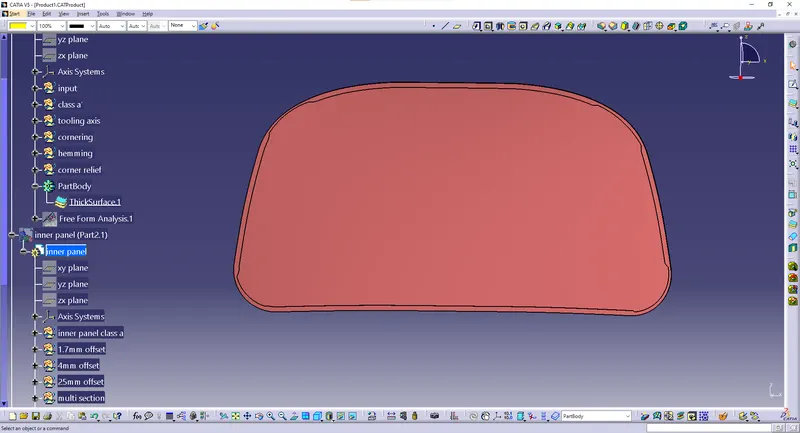
Hood inner panel:
Inner panel is the part that gives strength and rigidity to the outer panel. The master section represents the initial emboss shape and size. Then we provide the emboss for the latch and hinge elements after fixing the location.
Latch and Hinge reinforcement:
To furthermore reduce the impact to the occupants inside the car, additional latch and hinge reinforcement to the hood. When latch and striker are placed, there is drop in strength at that position thus reinforcement is required. Also stiffness pads are placed to reduce NVH. Hinge and latch reinforcement thickness is kept at 1.5 mm but it may vary.
Latch trajectory:
Latch trajectory is given by the circle drawn from the hinge axis point. Hinge axis point is the center point of the hinge axis. First, we can fix either the latch or the hinge. If we have fixed the hinge position then we should plot the Trajectory circle for the latch. For proper mating condition the striker axis through the tip of the striker should be tangential to the latch trajectory.
Deep Drawing:
Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered "deep" drawing when the depth of the drawn part exceeds its diameter.
Mastic point:
The Mastic point is an elastic compound that behaves like a rubber. The mastic points are defined on the hood inner panel where the hood can easily deform. They help the hood outer panel to come back to its original shape after it gets deformed. The mastic has an influence area of 80mm
Cornering:
Cornering is a process where the edge of the part is being cut in a way that there is no sharp edge in it.
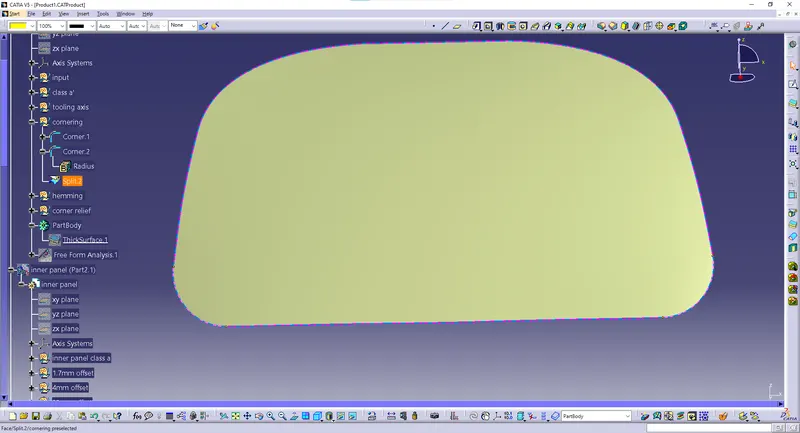
HEMMING PROCESS:
Hemming is a sheet metal forming process in which sheets are joined by bending it to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods and tailgates are formed by the hemming process. In this process, usually a sheet is bent with the help of an inner sheet in three different stages.
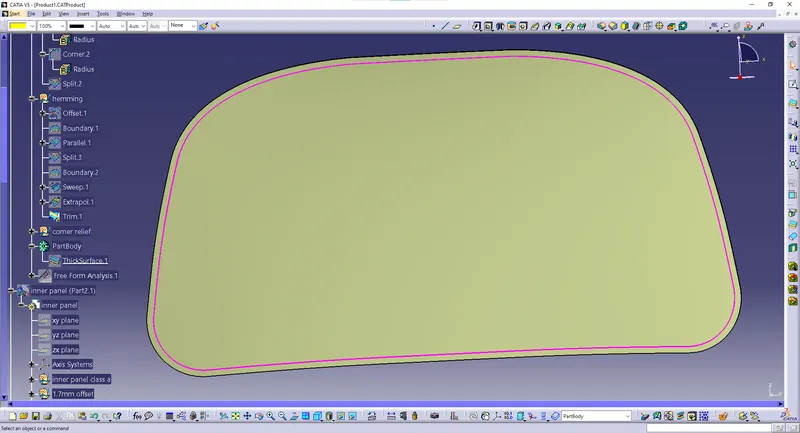
There are two types of hemming operations,
- Conventional die hemming
In conventional die hemming, the flange is folded over the entire length with a hemming tool.
- Roll hemming
It is the roll hemming process that is used for automotive sheet metals. Roll hemming is carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller which follows a defined path.
CORNER RELIEF:.
A bend relief is nothing more than two small incisions cut into a piece of sheet metal to free the metal between the two. It separates the material you want to be able to fold from the rest of the part. You only need it when there is material on either side of a bend.
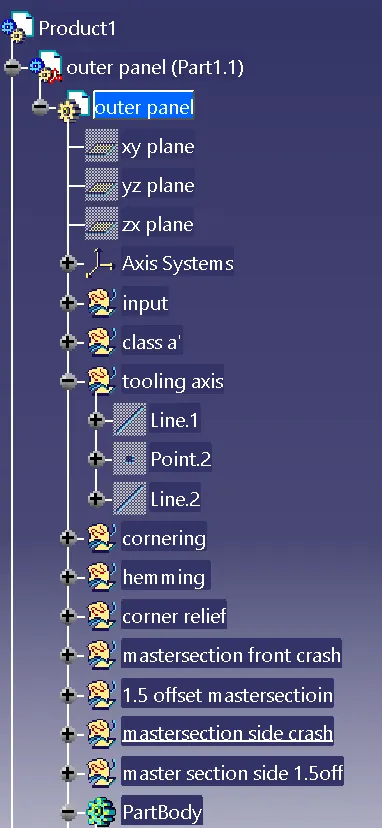
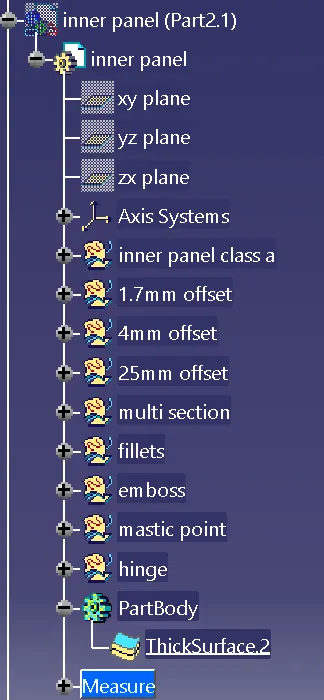
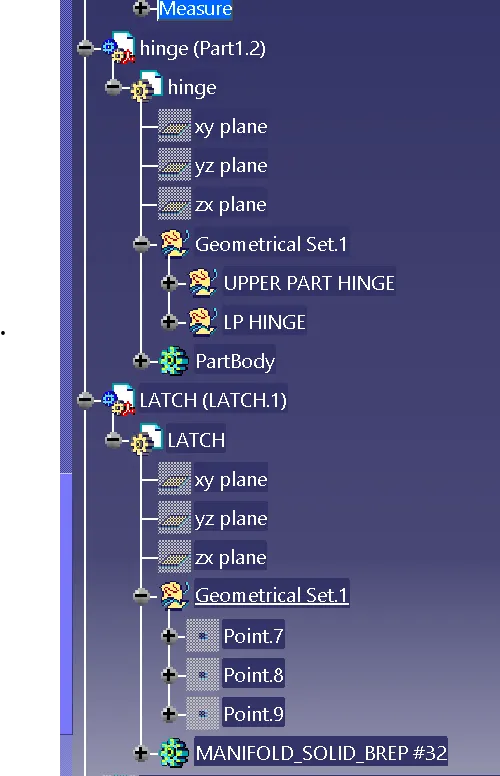
TREE STRUCTURE:
FINAL ASSEMBLY: