Design of backdoor
CAR BACK DOOR DESING
AIM :To desing back door pf car using given outer class A surface
WHAT is back door of car:
the door which is located rear said of the car which gives acc ess of boot space to storge luggage,spare wheels ect.thses back doors are can operated manually and electric powered.
TYPES OF BACK DOORS WITH WORKING POSITIONS:
- TOP MOUNTED DOORS
- SIDE MOUNTED DOORS
- BOTTOM MOUNTED DOORS
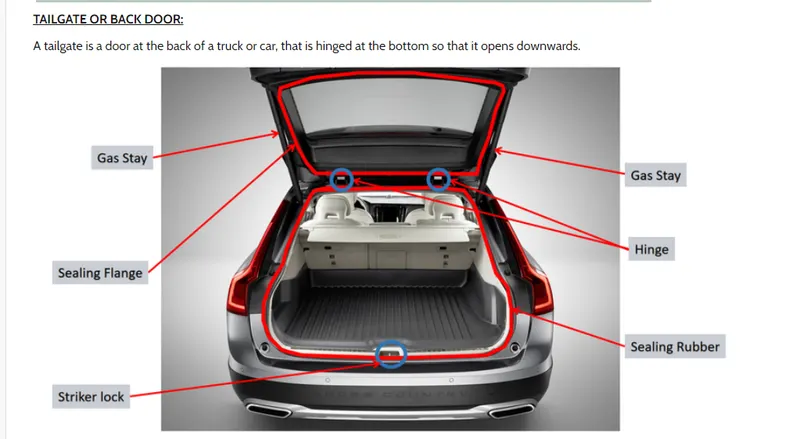
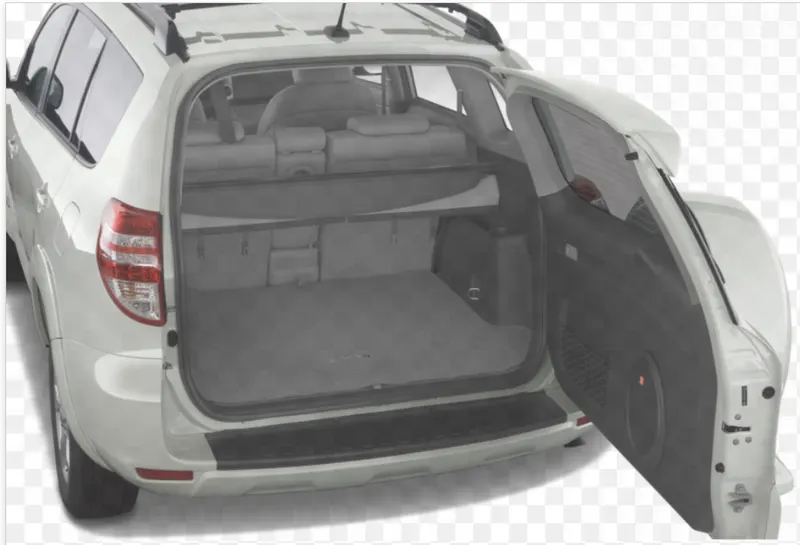
this is said door
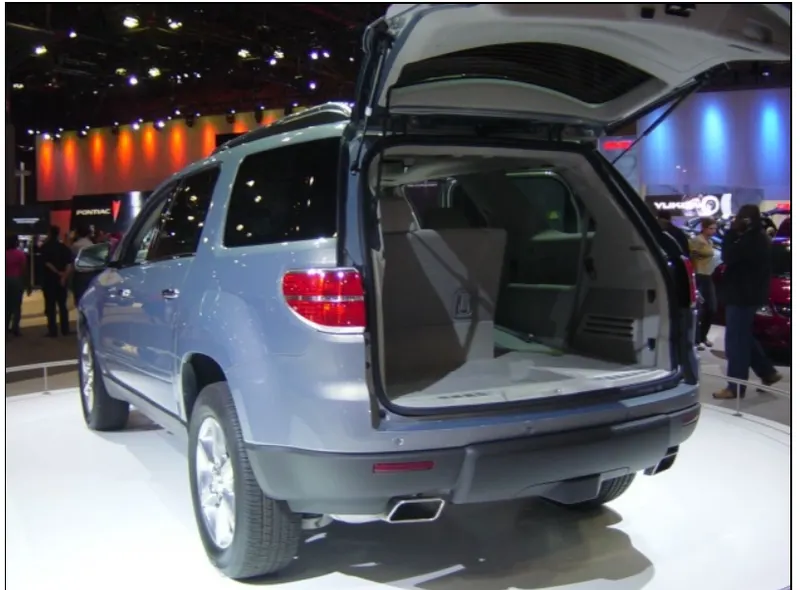
these are the few types of back door images.
BACK DOOR ASSEMBLY PROCESS:
inner panel
outer panel
gas saty
wiper motor and reinfrocement
hinge and its rein reinfrocement
THE few cad tools are used in he assembly of the back door.
DEEP DRAWIMG
metal deep drawing process is an effective method of manufacturing of cuos,cans and other similar drawing products.the deep drawing having two main categories
- first stage drawing
- redrawing
FIRST STAGE DRAWING: the shape of metal is placed on the die and contact with the punch.when the metal secimen is flat piece of sheet metal uesd in forming and finish product.initially the punch moves downword dirction.the outer rim of blank subjected to pure radial drawing between the die and metal blank.the metal become bend and slide the over die stretched between die and punch.the metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
REDRAWING :the compoments draw for the first stage again it is redraw convert into more depth to form a cup shape in the die and punch.
it is called as the redrawing.
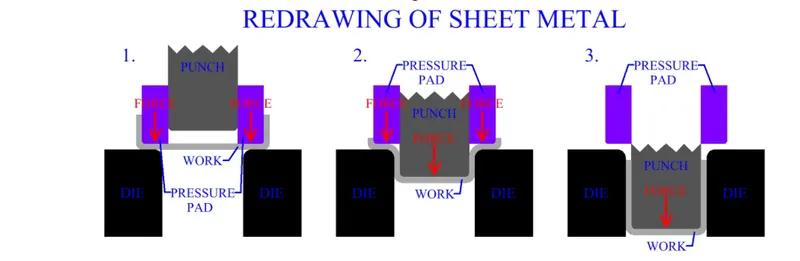
EMBOSSING PROCESS
embossing is a metal forming process for producing raised or sunken desing or relief in sheet materials by mmeans of matched male and female roller dies.theoretically with no chane in metal thickness or by passing sheet or astrip of metal between rolls of desing pattern.
materials commonly used in the metal embossing process include
- aluminum alloys
- steel alloys
- zinc
- copper
- galvinized steel
- brass
- cold rolled steel
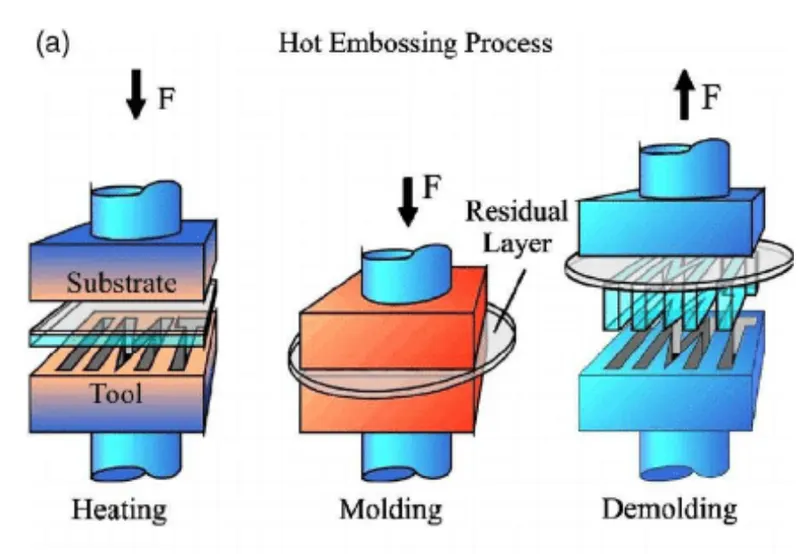
THIS IS THE ONE TYPE OF EMBOSSING PROCESS.
HEMMING: hemming is aforming operation in which the edges of the sheet are folded over another part in order to achieve atigh fit normally
hemming operation are used to connect parts together to improve the apperance of a part. in car part production hemming is used in assembly as a secondary after deep drawing.trimming and flangeg operations to join two sheets metal parts.
there are varius types of hemming operations:
- CONVENTIONAL DIE HEMMING : conventional die hemming is the flange is floded over the entire length of hemming tool.
- ROLL HEMMING:in roll hemming,the hemming roller is guided by an industrial robot to form the flange
- OPEN HEMMING:ahemming has afull round feature and a return flange in open bend angle.
- TEAR DROP HEMMING:in tear grop hemming the bend angle is greater than 180 degrees.
- CLOSED HEMMING: closed hemming is without any inside radiu
BLANKING
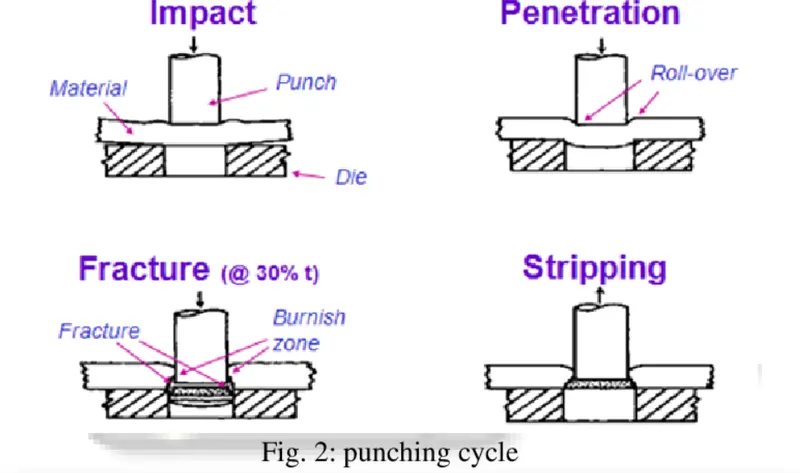
blanking is a cutting operations of a flat metal sheet artical punched out is valled the blanking.
PUNCHING
it is same as the blanking process. the hole is requied product and material is punch out form the hole is take as the wast material.
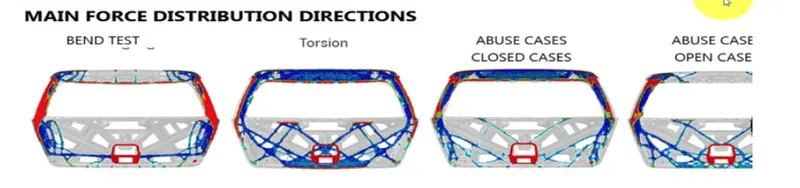
FROCE DISTRIBUSTION IN BACK DOOR
BACK DOOR DESING IN NX CAD
door parts and thinness is given
inner panel=0.75
outer panel=0.75
reinfrocement=1.5
given data
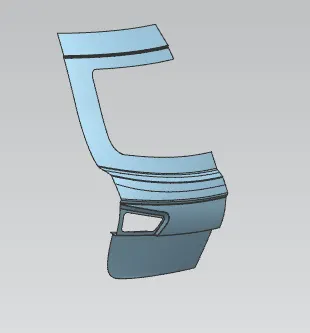
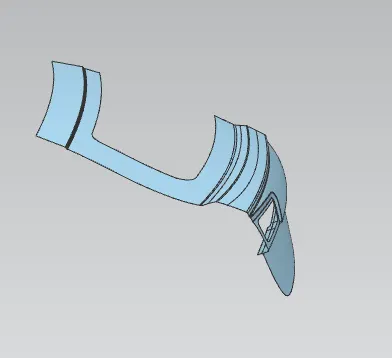
given surface has to be reparied according to the smoothness after repariing the surface is divided into two parts back door outer paneland back door inner panel.
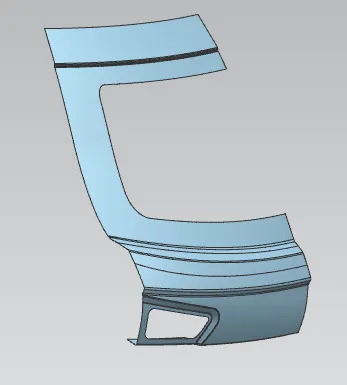
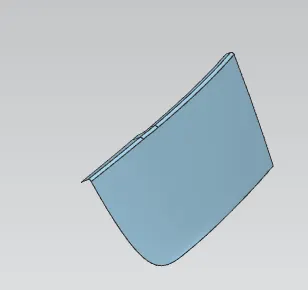
first we need to creat the tooling direction for deep drawing. it will helps as to making of the back door.
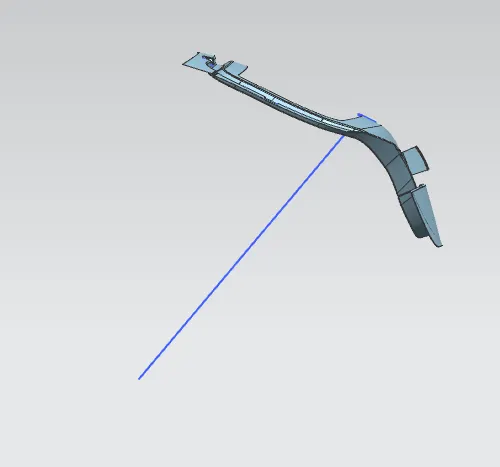
after that we are creating the seling fiange by offseting thr outer panel.
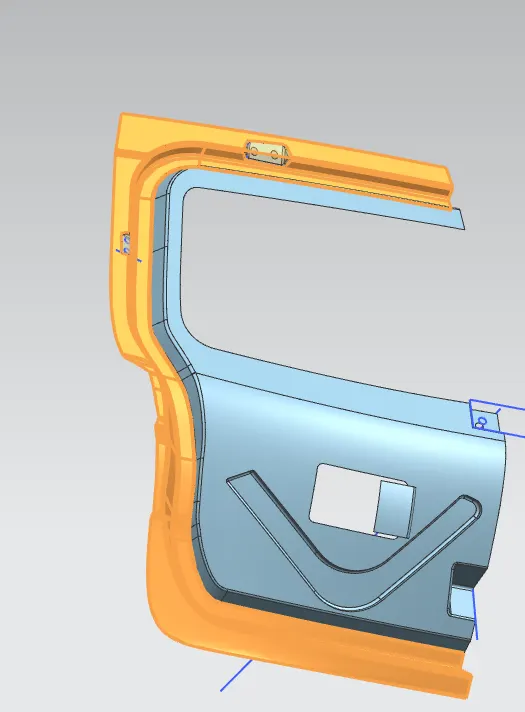
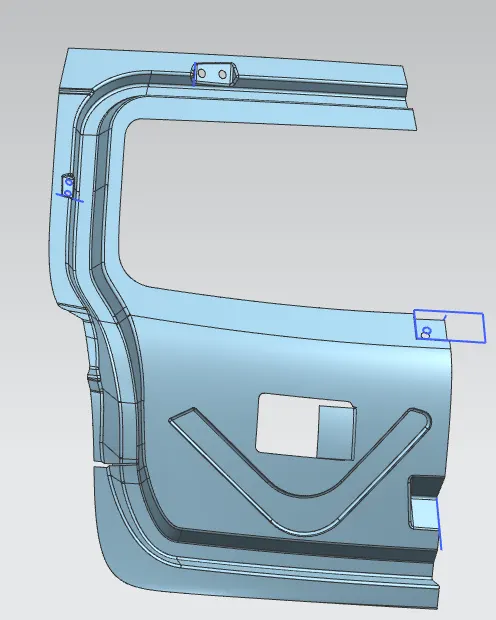
than we are creating the back door inner panel
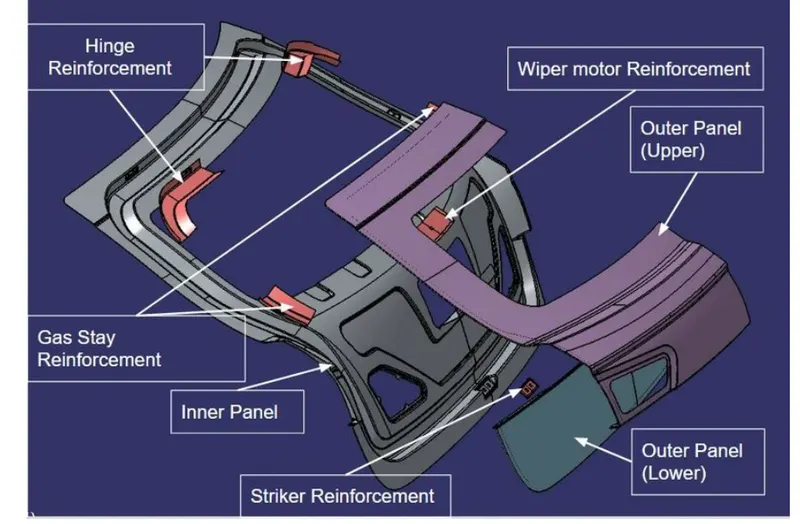
reinfrocement
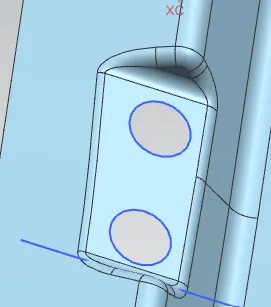
thicken process
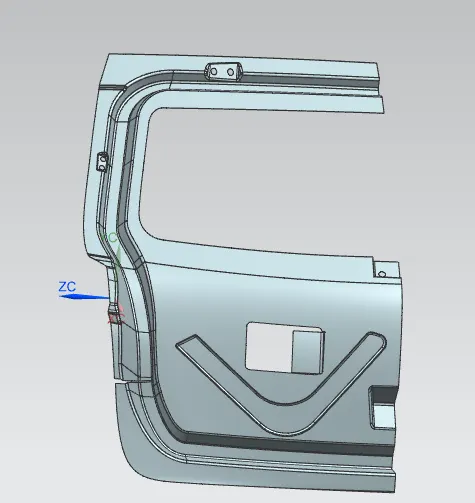
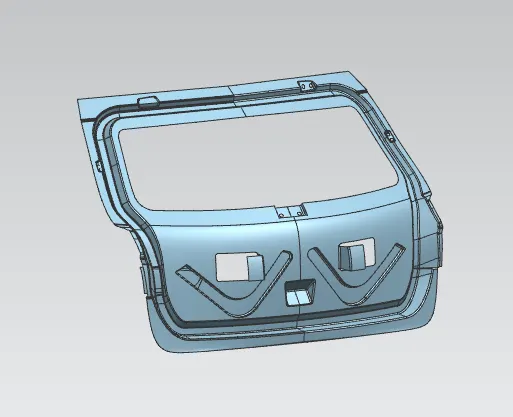
after the assembly of the back door of inner panel parts.
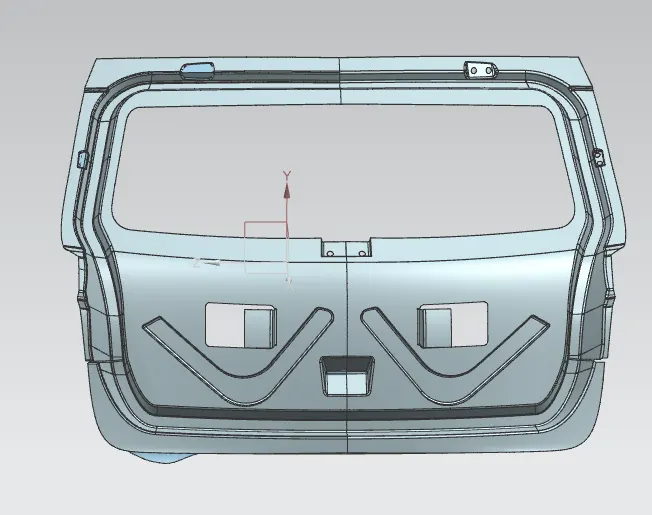
the thicken is done on the surface with the value of 0.75.
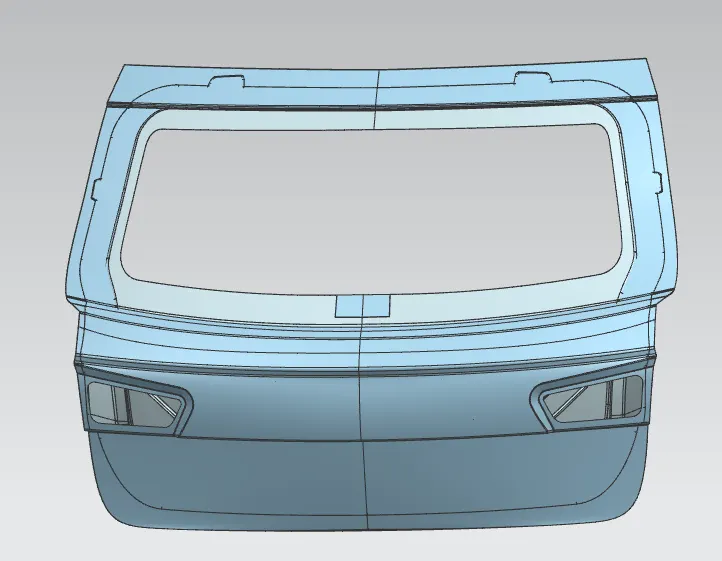
the total assembly of the back door
conclustion:with the help of the given data and the dimensions we did the assembly of the bach door.we did the thicken and embossing and the reinfrocement of the parts