DESIGN OF CAR TAILGATE & ASSEMBLY
DESIGN OF CAR TAILGATE & ASSEMBLY
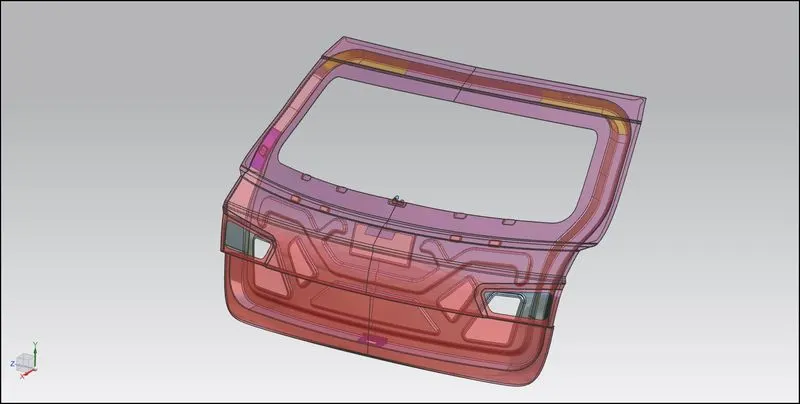
Objective:
- For a given backdoor styling surface Come up with a design of the inner, outer panel of the tailgate with essential reinforcements and flanges required.
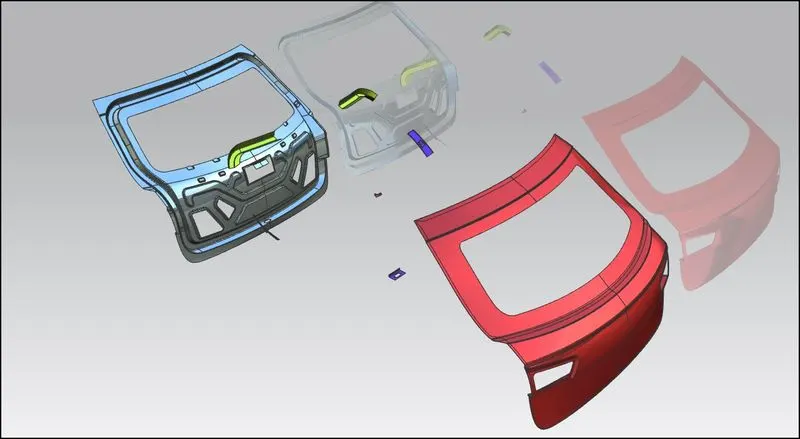
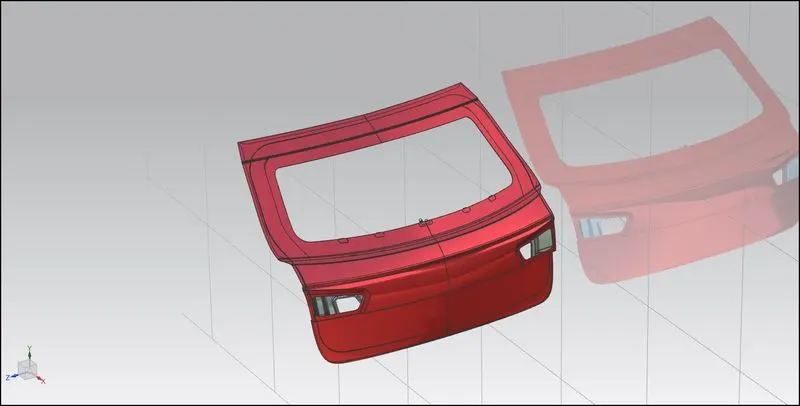
- To create a complete tailgate by assembling all the components altogether.
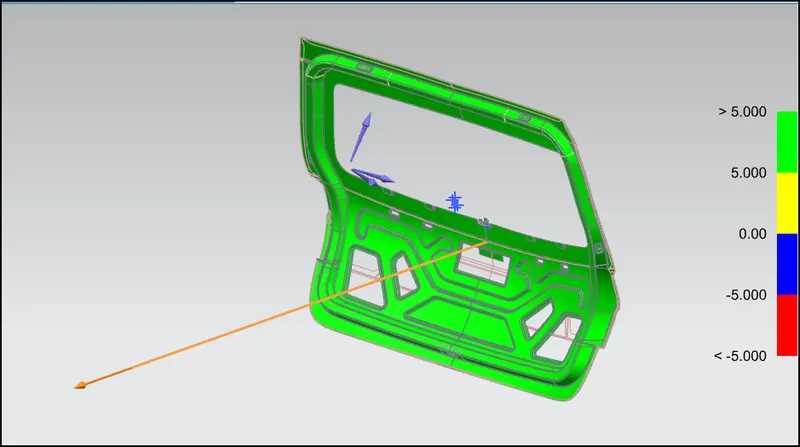
- To perform draft analysis on the various components of the tailgate, to ensure that they are manufacturable.
1.0 Introduction:
TAILGATE/BACKDOOR OF A CAR
- The Backdoor is an automotive component that is located at the rear side of the car which covers the back portion of the car body it is also known as the tailgate. It is located next to the rear passenger seats and it gives access to the luggage space by opening it in an upward direction, it is also called a trunk compartment as it provides space for storage of goods and luggage. If the rear door is mounted on top then it is called a tailgate, it is mostly used in station wagons, Sport utility vehicle and hatchback-type cars.
- The opening of the backdoor depends upon the type of vehicle the different types of rear door opening are as follows:- Side-mounted, Top-mounted, Bottom mounted.
- Two-way station wagon tailgates may be hinged at the side and the bottom so they can be opened sideways like a regular door, or drop downwards as load platform extenders. They are designed with special handle(s) for opening in the selected direction on special hinges after the window is lowered.
- Nowadays the modern cars come up with power-lifted tailgates that is it consists of electric motors to open the tailgate which require only initial force to activate and then it get opened automatically. In some cars, foot sensors are provided which senses the foot movement to open the tailgate. This type of system is used in premium cars and it eliminates the manual opening of the tailgate.
Fig.1.1 Different variants of Tailgate Mountings
2.0 Manufacturing process of Backdoor
As we know that backdoor is a BIW component that is basically manufactured using a metal forming process. There are different types of metal forming processes that are used for manufacturing automotive parts they are bending, forming, stamping, forging, extruding, etc. From which the stamping is the methodology used to produce the door panels, basically, a die and punch are used in a press machine to stamped out the complete door panel in a single or multiple presses. This method is used because it does not require separate tools to manufacture the component also it is less time consuming and requires less material for the part which is to be produced with precision and accuracy.
Materials used for the manufacturing of backdoor panel
The functional requirement of a backdoor panel is it should be light in weight but in contrast, it should have sufficient strength at the same time to fulfill these requirements the two types of material are used
1) Aluminum
2) Steel
The first one as we all know that it is light in weight compared to that of steel but at the same time the price of aluminum is more than that of steel. So, it is only used for expensive cars or sport vehicles where the weight of the car plays a crucial role. The manufacturing process used for panels made up of aluminum is different when compared to that of steel.
Aluminum panels are made by casting process rather than stamping which is used for steel material due to which the accuracy and precision of the panel is more as compared to that of steel. We can provide sufficient strength by varying the thickness of the sheet at weaker sections in the case of aluminum no reinforcements are needed to be provided but in steel panels, reinforcements are essential as we can not vary the thickness of the sheet it is uniform throughout so, steel panel requires more components as compared to that of aluminum. These are some of the advantages of aluminum over steel.
But the drawback of aluminum is it requires more cost to produce a single panel when compared with steel. So, it can't be used all cars but used for luxury cars only.
To overcome the drawback of steel recently a new method is used for manufacturing i.e is Ultralight steel auto body concept this method gives two ways to reduce the weight of the steel
1) Hydro-Forming
2) Tailor welded blank
Hydroforming
Hydroforming is a cost-effective way of shaping ductile metals such as aluminum, brass, low alloy steel, and stainless steel into lightweight, structurally stiff, and strong pieces. Hydroforming is a specialized type of die forming that uses high-pressure hydraulic fluid to press room temperature working material into a die. To hydroform aluminum into a vehicle's frame rail, a hollow tube of aluminum is placed inside a negative mold that has the shape of the desired result. High-pressure hydraulic pumps then inject fluid at very high pressure inside the aluminum tube which causes it to expand until it matches the mold.
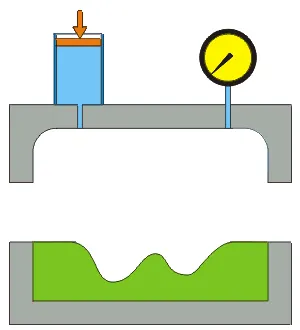
Fig.2.1 Hydroforming Process
3.0 DESIGN CONSIDERATIONS FOR BACKDOOR
Before starting with designing we should take into account the design protocols which are to be followed while designing. In the case of the backdoor following are the design parameters
1) Rear visibility criteria
2) Rear Crash regulations
3) Functions of sealing
4) Joining techniques used like heming, spot welding
So, above are some of the design constraints that are to be followed in design the first one is the most important as it directly relates to the safety of the driver. The backdoor should be designed in such a fashion that the driver should be able to see the rear objects clearly i.e the scope of rear visibility should be maximum it should not get hindered by the backdoor body.
While designing this criterion should be followed and the maximum area should be covered by rear windshield glass for better visibility of the driver and his safety.
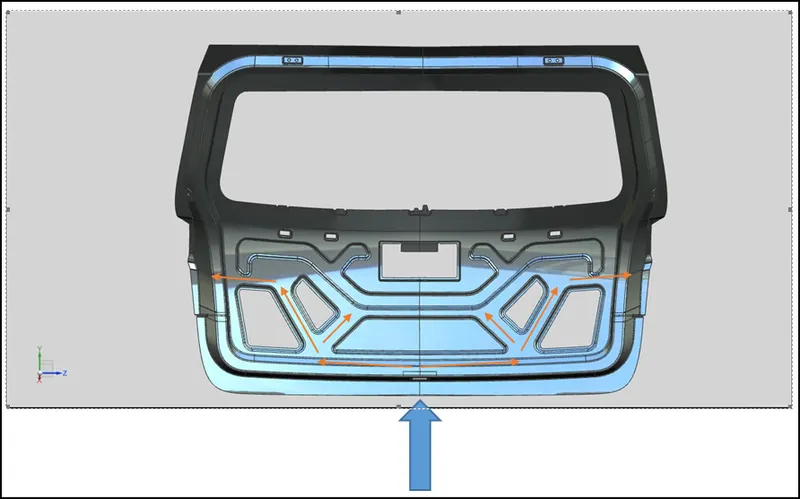
Next is the rear crash conditions so, the designer should also take a look at this parameter the outer panel should have sufficient strength that in case there is an impact from the rear side then the outer panel should take a maximum of load and allow less load to be driven towards passengers thus protecting them from any fatal injury. For that purpose, a design engineer can use an inner panel to strengthen the structure of the back door. Embossed sections are created on the inner panel is generally V & Y shape to deviate the forces in an outward direction rather than directly in the normal direction.
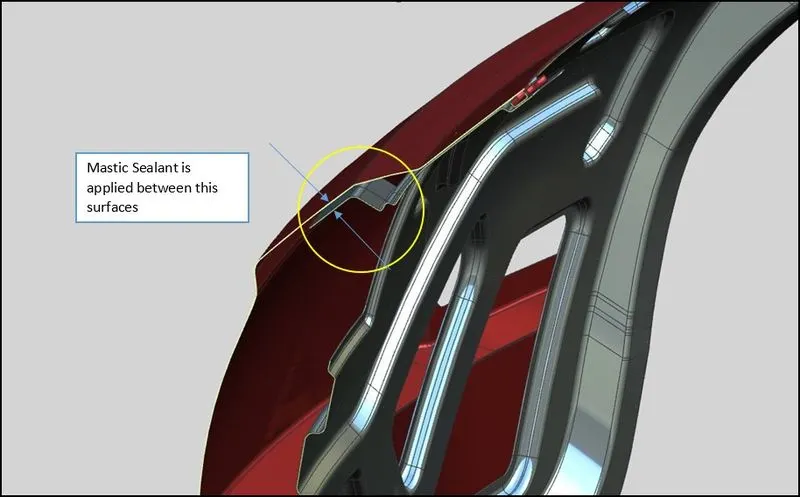
Proper sealing is also to be provided in between car body and backdoor thereby not allowing any foreign material to get inside the storage space, that is sealing prevents water, dirt, dust to get in the storage space. So, proper rubber sealing is to be provided on the car body, and a sealing flange is provided on the inner panel of the backdoor which gets in contact with the rubber sealing and forms bound when the door is closed.
Load Analysis of Backdoor
1) Bend Test
2) Torsion
3) Abuse case
4) Dent test
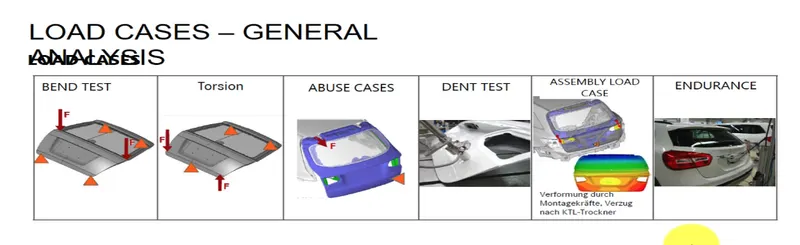
3.1 Load Analysis of Backdoor
Joining Processes used in Backdoor assembly
There are different joining processes that are used in the assembly of backdoor such as heming, spot welding etc.
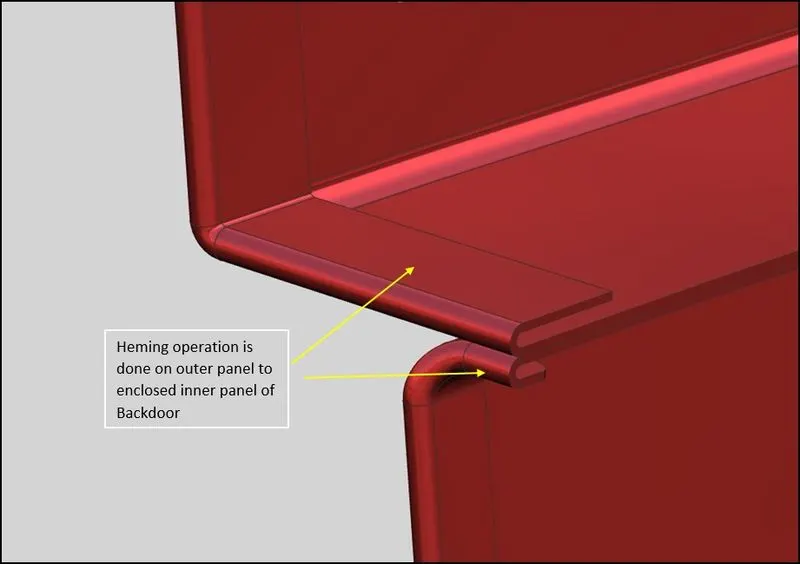
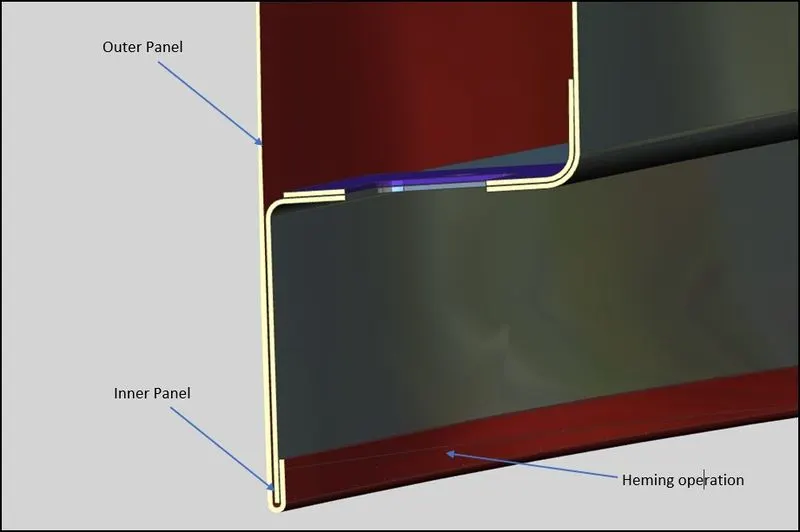
Hemming:- It is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In-car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
3.2 Heming Operation
Spot Welding:-
Spot welding is a type of electric resistance welding used to weld various sheet metal products, through a process in which contacting metal surface points are joined by the heat obtained from resistance to electric current
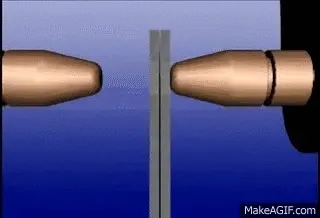
3.3 Spot welding demonstration
4.0 ELEMENTS OF BACKDOOR
Backdoor is again an assembly it is not a single part it consists of two panels one is an outer panel and the other is an inner panel the inner panel is enclosed beneath the outer panel of the back door and in between these sheet metal bodies other components are located.
Assembly of Backdoor
Different panels of backdoor
1) Outer panel upper
2) Inner panel
3) Outer panel lower
Other components of backdoor
1) Hinge reinforcement
2) Wiper motor reinforcement
3) Gas stay mounting reinforcement
4) Latch & striker reinforcement
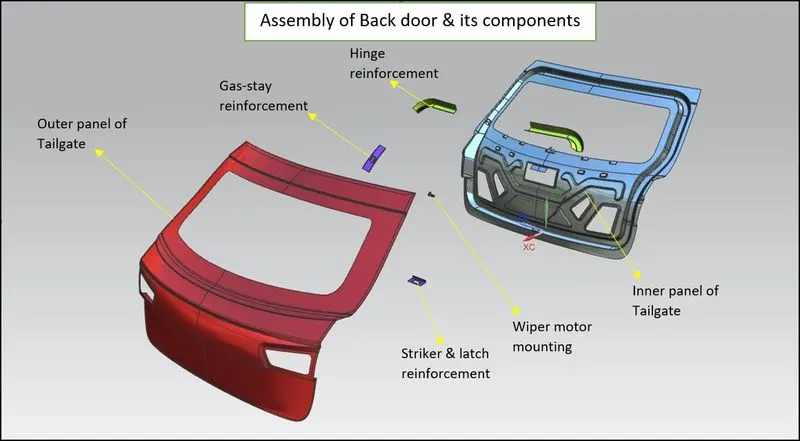
4.1 Assembly of backdoor & its various components
Outer Panel upper -
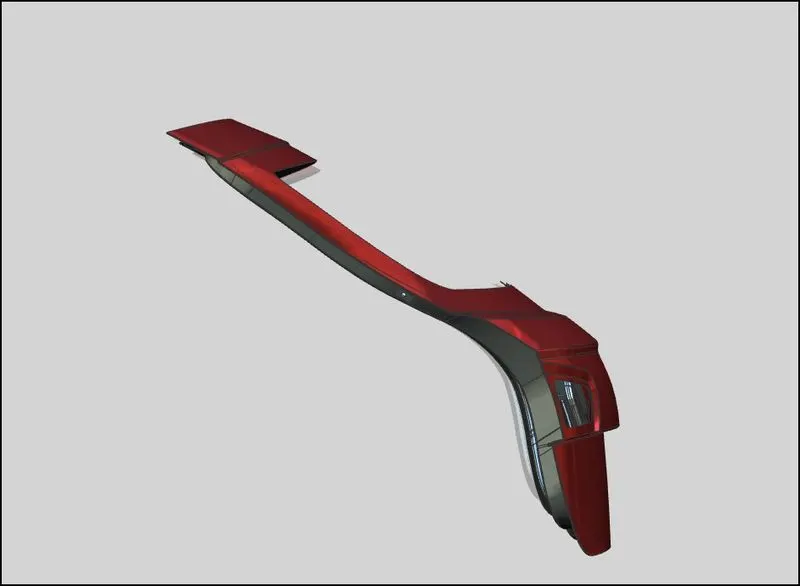
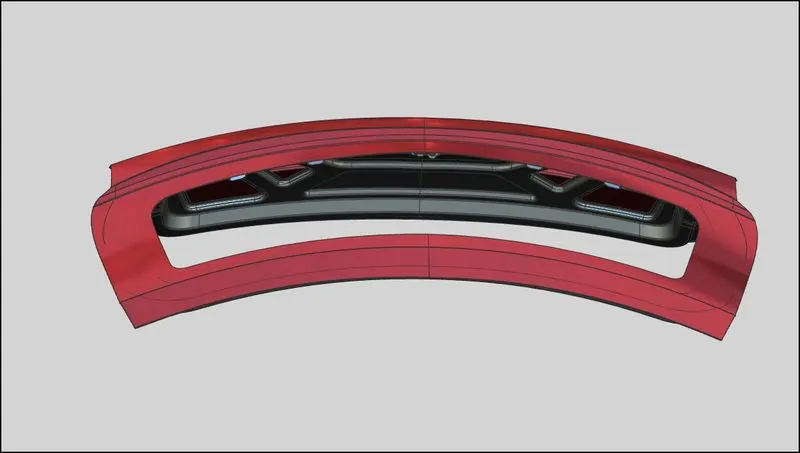
Forms the outer covering of the Backdoor with other elements enclosed beneath it, It provides sufficient strength to the car by covering it from the rear side it also increases the aesthetic look of the car. It consists of cutouts for the fitment of rear tail lamps, fog lamps, etc. Again the outer panel is a BIW component and as discussed earlier it is manufactured in a single piece operation by using stamping operation. The steel sheet is paced above the negative die which is having the desired shape and then punch is forced to hit the steel sheet with heavy load acting in a normal direction thus, it expands the steel sheet to the shape of the negative die and desired part is taken out.
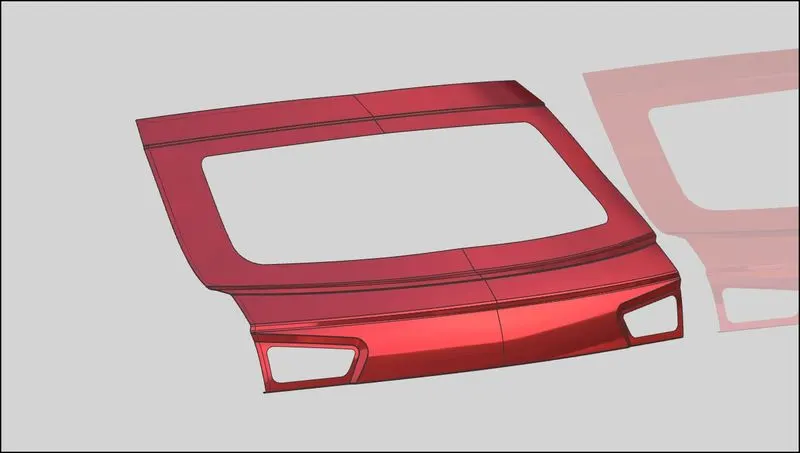
Fig.4.2 Upper Outer panel of backdoor
Inner Panel-
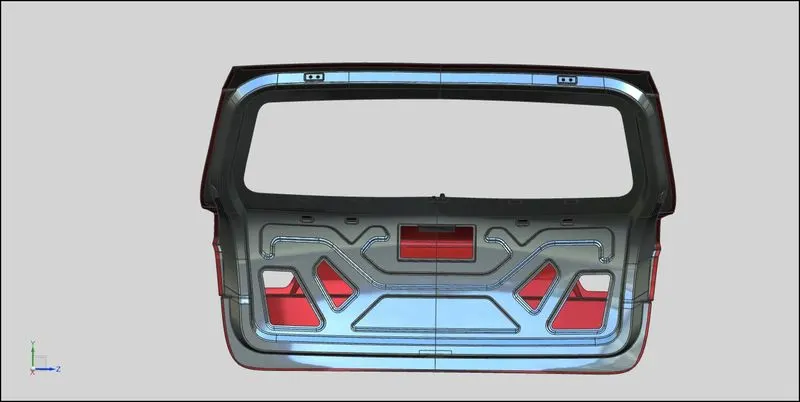
It is located on the inner side of the outer panel the main purpose is to provide further strength and all the components such as wiper mounting, hinges, gas stay, latch, and striker reinforcements are all fixed on the inner panel that's why it is very important that the inner panel should be sufficiently strong enough to carry all the load of this components and also strengthen the structure to safeguard the backdoor from the rear crash conditions. The process used for manufacturing of inner panel is generally deep drawing it is similar to that of the outer panel, a tooling direction is to be decided in which the punch will act upon and apply load on the metal sheet to deform it in the desired shape. Embosses are also provided on the inner panel to transfer the force away from the center to the sealing flange and other body members.
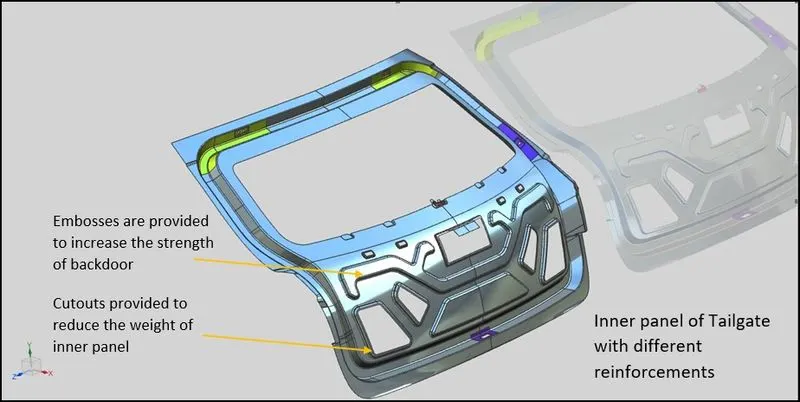
Fig.4.3 Inner panel of backdoor
Outer Panel Lower -
It is located just below of upper outer panel it is manufactured separately and afterward joined with the outer panel by using joining methods like spot welding as explained earlier. Heming operation is also carried out on the edges of the outer panel so that it gets fit with the inner panel sheet. Mostly Car number plate is located on the outer lower panel.
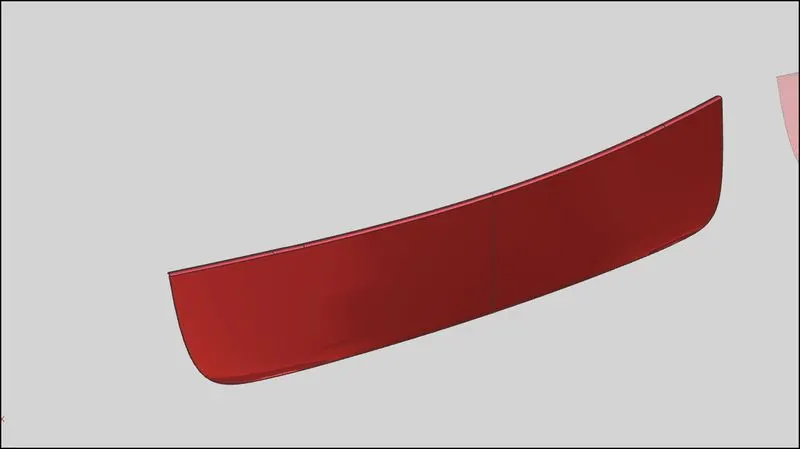
Fig.4.4 Lower outer panel of backdoor
5.0 Other components of Backdoor
The above are the main parts of backdoor assembly other than these components their are various parts that are located inside the backdoor assembly they are
1) Hinge reinforcement:- This is provided on the inner panel to provide strength to the inner panel and to carry the hinges which are to be mounted.
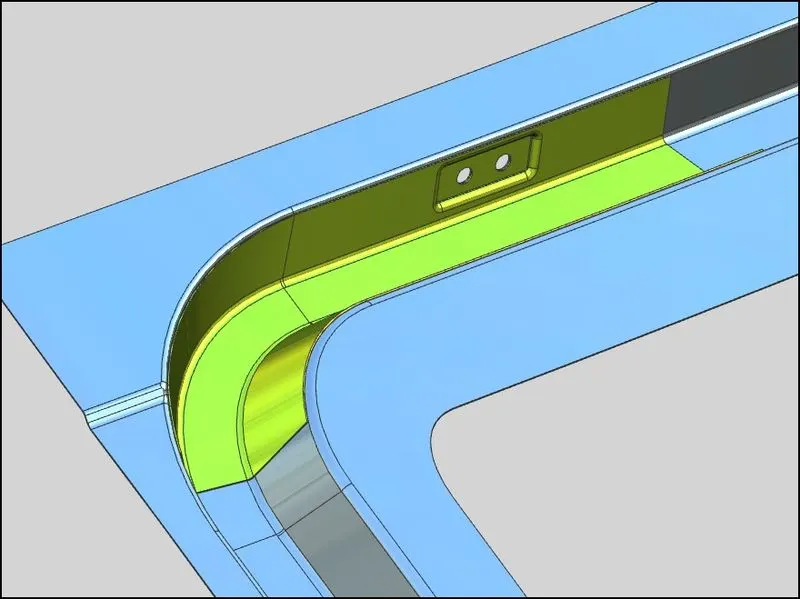
Fig.5.1 Hinge reinforcement
2) Wiper motor mounting Plate
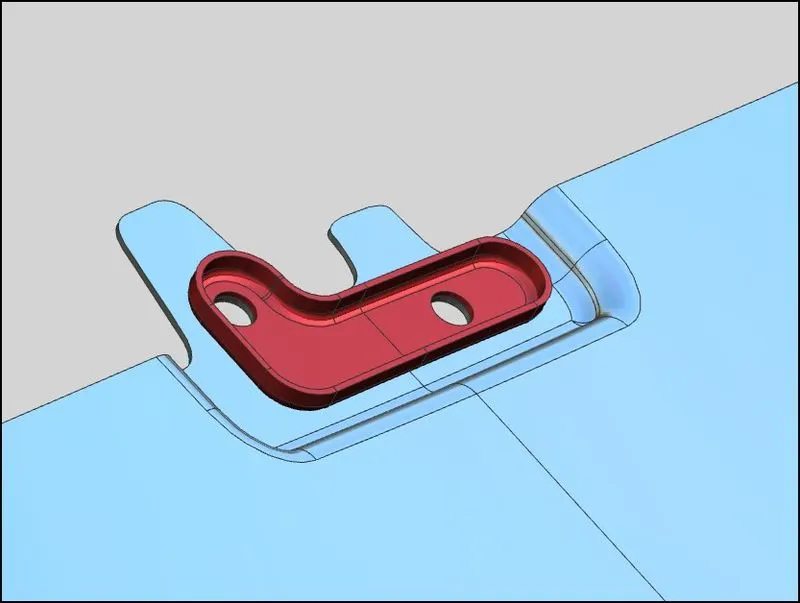
3) Gas stay mounting reinforcement
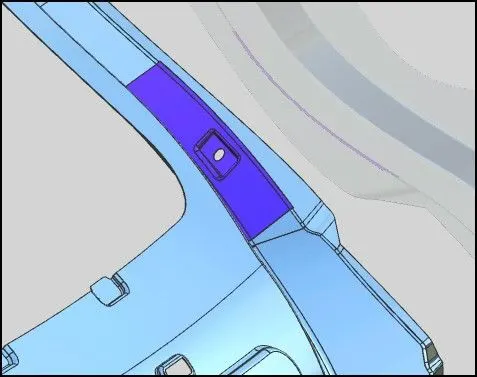
4) Latch & Striker reinforcement
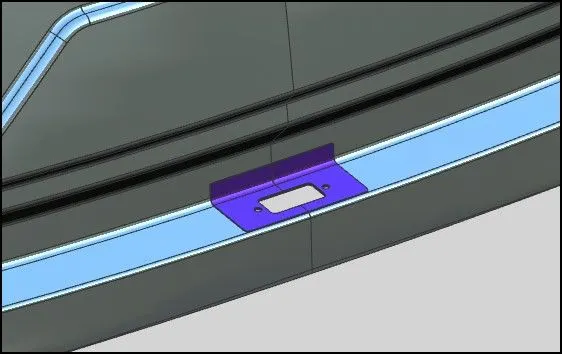
6.0 Ilustration of Heming Process
7.0 Force Distribution
8.0 Position of Hinges, Latch & Striker
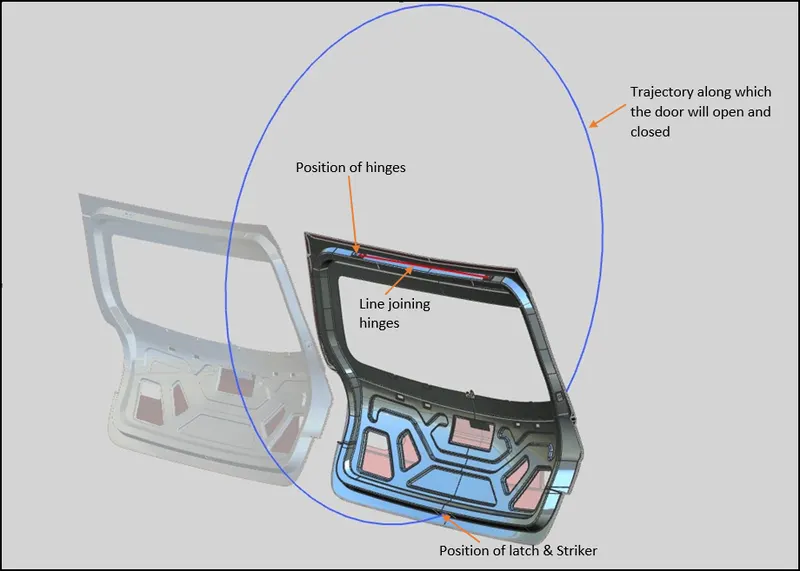
This position is decided by taking the center point of hinges and drawing an axis joining this point of hinges then drawing a circle by taking the midpoint of the axis as the center of circle and endpoint as a point of latch & striker. This gives us a trajectory on which the back door will open and closed.
9.0 Draft Analysis
# 1. The inner panel of Backdoor
10.0 Final Images of Backdoor
CONCLUSION:
- Successfully completed the design and assembly of the backdoor with its functional components.
- Learned the importance of backdoor and its manufacturing processes.
- Carried out Draft analysis to determine whether the part is manufacturable or not.
- Learned about Design considerations taken into account while designing.