Design of backdoor
Back Door
Back Door or Tail Gate is one of the BIW Component in a Car. For some cars it gives access to the boot space where the luggage and other goods can be kept. In case of some big cars there is a seating arrangement in place of boot space for which back door becomes the entry gate.
Some doors needs to be lifted and closed manually while few cars have the facility to operate the door by a remote or by electrical or sensor means.
Some doors are mounted on the vertical flange and are known as side mounted doors while others mostly mounted on horizontal flange are knows as Top mounted doors.
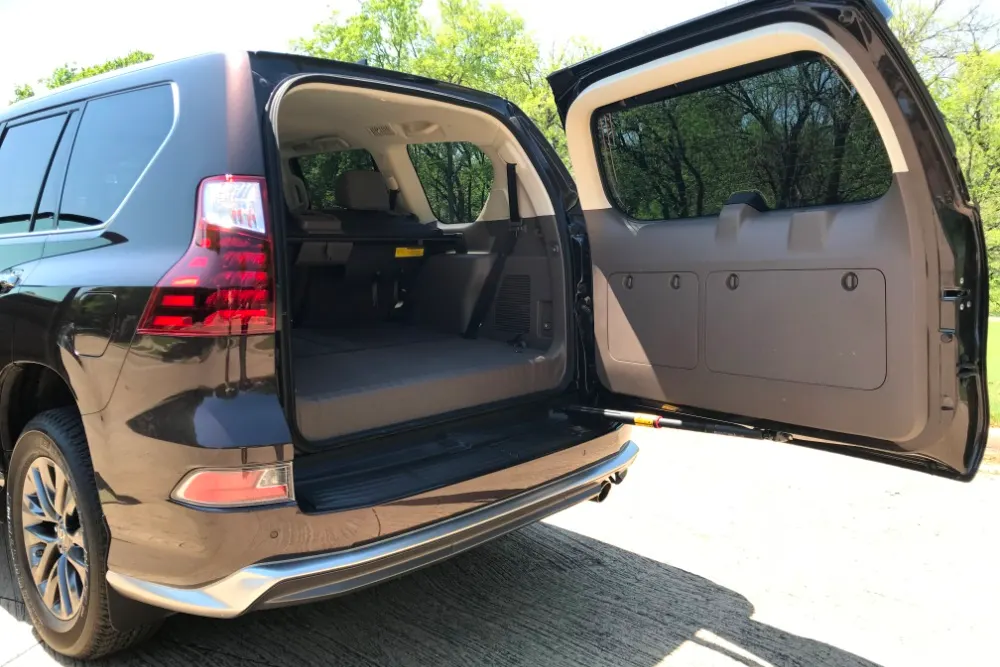
Just like hood of a car the backdoor also have an inner panel. It has hinges for opening and closing of the door. To facilitate the opening of the tail gate and keeping it in open position there are Gas Stays attached to the Tail Gate on both the sides whose one side is attached to the back door and other to the car body.
Hood and Front Windshield are completely separate communities but in case of a back door. The rear windshield is housed in the back door itself. As it have windshield so it needs wiper too for the same purpose as front windshield. So there is an arrangement for wiper motor as well.
Back door also facilitates the fixing of Tail Lamps and the License plate over it as well in most cases.
Apart from that for closing of back door there is a latch and striker arrangement. The trajectory of this moment of Striker also needs to be defined in designing so that a proper lock can be achieved.
Parts Of Backdoor Assembly
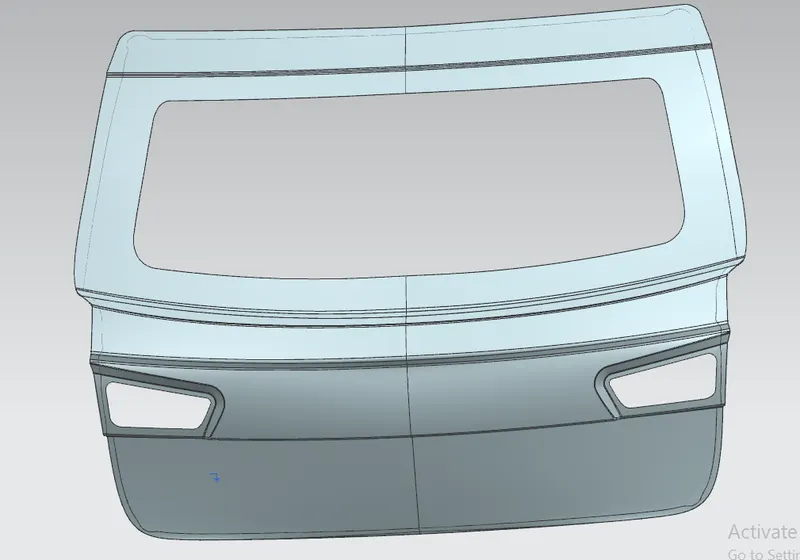
Back Door Outer Panel :-
It is the metal covering of a back door. Generally Structural steels are used as a material for back door outer panel but now Aluminium alloys are also used because of its light weight. IN most cases the Tail Lamps and License no. plate is attached to the outer panel itself.
Back Door Inner Panel:-
It is the most important part of hood assembly. It is situated between the hood outer panel and the boot space. Basically It is like a shadow of Backdoor outer panel but before it attached to the backdoor outer panel or applied to the location lots of operations are done on it to bring some definite changes in order to get the desired effect. In most of the cases its material is same as that of backdoor outer panel such as Structural steel, Aluminium, Carbon Fibre etc. The distance between back door inner Panel and outer panel is not uniform throughout its length. The hemming reason have very small distance almost 0.2mm for oozing out the sealant. The distance is relatively very large at some portions where tail lamps or wiper motor is to be mounted. Apart from the hemming inner and outer panel are attached by mastic sealants which along with joining them increases the the strength locally and holds them together.
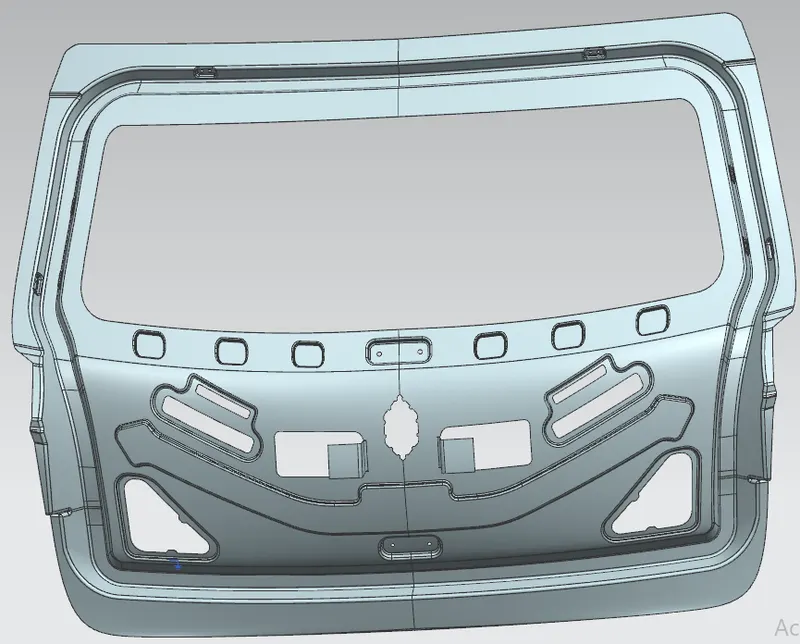
We can remove/trim some material from the inner panel for the weight reduction purpose. Inner Panel also have a sealing flange which runs through the side of inner panel over which a sealant or rubber material is attached. At opening position of tail gate it has its normal volume but when the tail gate is closed it squeezed. It is used to prevent water from entering the boot space where the luggage and other goods might be affected by water. It is completely sealed once it gets closed.
To avoid the severe consequences of a collision from back side with backdoor of a car on inner panel there are embosses which are also referred as Y embosses so that the force of collision can be dissipated away from the backdoor. Emboss is a raised design or mark on the surface of Inner Panel. On the inner panel we add more embosses to enable the stiffness of the car. Whenever a collision happens force willl go straight to the the bot space or sitting compartment So to reduce the force Embosses are employed. Embosses dissipates that force outside the car the design and shape of embosses are such that the direction of force changes to away from the center Apart from this embosses also increase the moment of inertia of inner panel which in turns increases the strength as well.
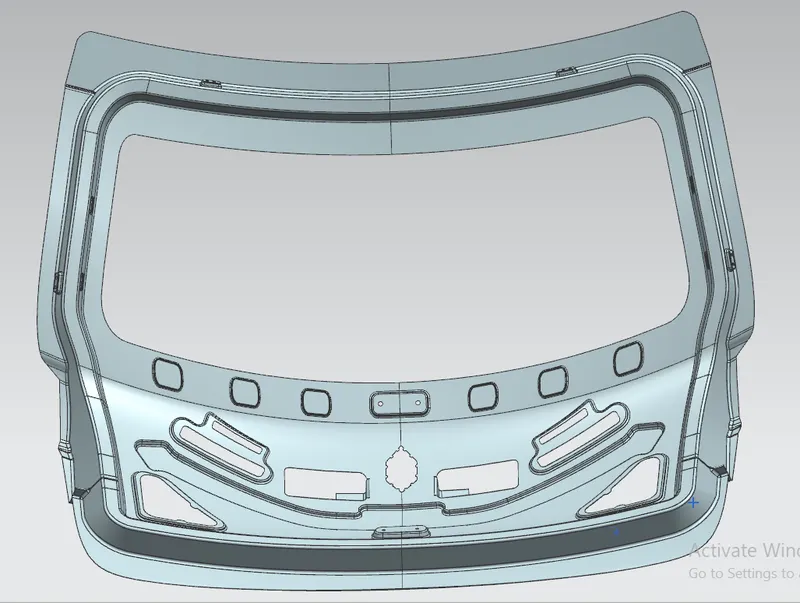
One such consideration is while trimming the sheet for any purpose other than weight reduction embossed surface around the trim portion are suggested if we punch a functional hole on a flat surface there are chances that the flat surface might tear off so to avoid that condition embosses are used which avoid this tearing situation. A functional hole is such where there will be other commodity attached to it for some definite operation/function such as holes in hinge emboss.
Reinforcements:-
Whenever we add any part or weight over another component the component loses strength so to compensate for that lost strength we employ the reinforcements. Reinforcements thickness is generally more than the thickness of the inner or outer panel. In case of Aluminium backdoor we do not need separate reinforcements because aluminium can be casted and at the zones where there will be an additional community attached to it the thickness of backdoor panel is increased to accomodate for the desired strength. In case of steel there are separate reinforcements for many parts which are as follows:-
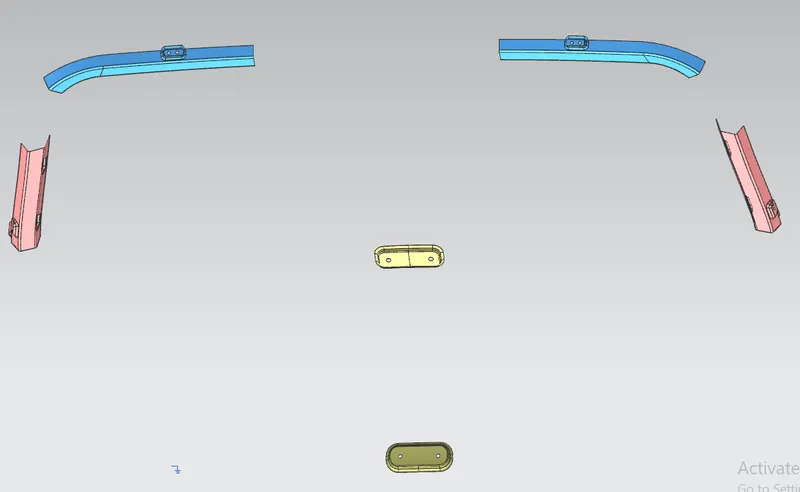
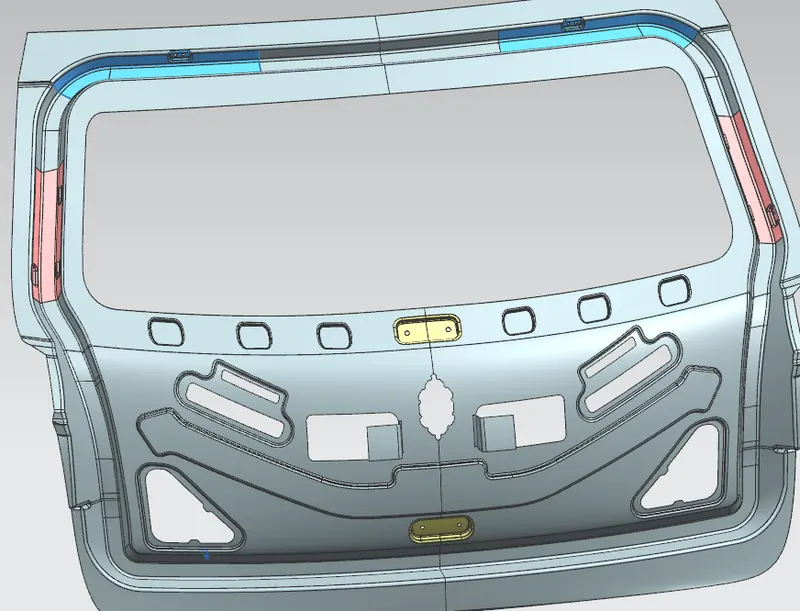
- Latch or Striker Reinforcement:- Firstly it needs to be determined that among latch and striker which part is going to be mounted on the tail gate of a car and according to that emboss is created on the tail gate and over that emboss reinforcement is placed to provide the strength. Its thickness can be 0.75-1.5mm
- Wiper Motor Reinforcement:- For the rear windshield wiper is a necessity which is actuated by the motor which is mounted on the tail gate inner panel. So first an emboss is made after that reinforcement is attached to it.
- Gas Stay Reinforcements:- For opening the tail gate and keeping it still in that position gas stays used on both sides. One side of gas stay is attached to the inner panel and to give that region of inner panel an extra strength we provide a reinforcement over the gas stay embosses
- Hinge Reinforcement:- Similar to hood tail gate of a car is opened and closed in a similar fashion and it is made possible by the hinges. Hinges are mounted over the hinge emboss which are supported by the hinge reinforcement.
Draft Angle:- We get a draft angle from the production team and all the components designed or modified in the BIW component should have a positive draft so that the punching tool can come out easily after operation.
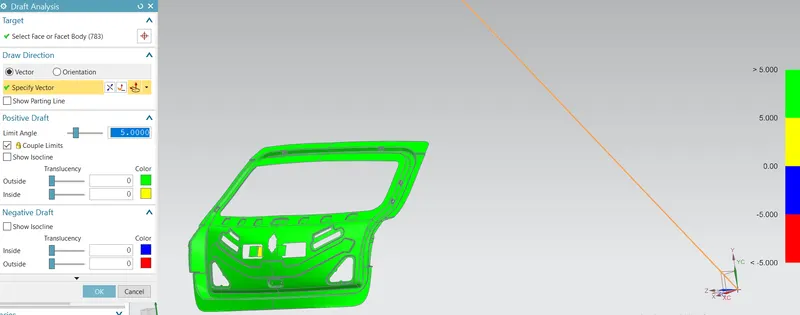
The Draft Analysis command enables us to detect if the part we drafted will be easily removed. This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
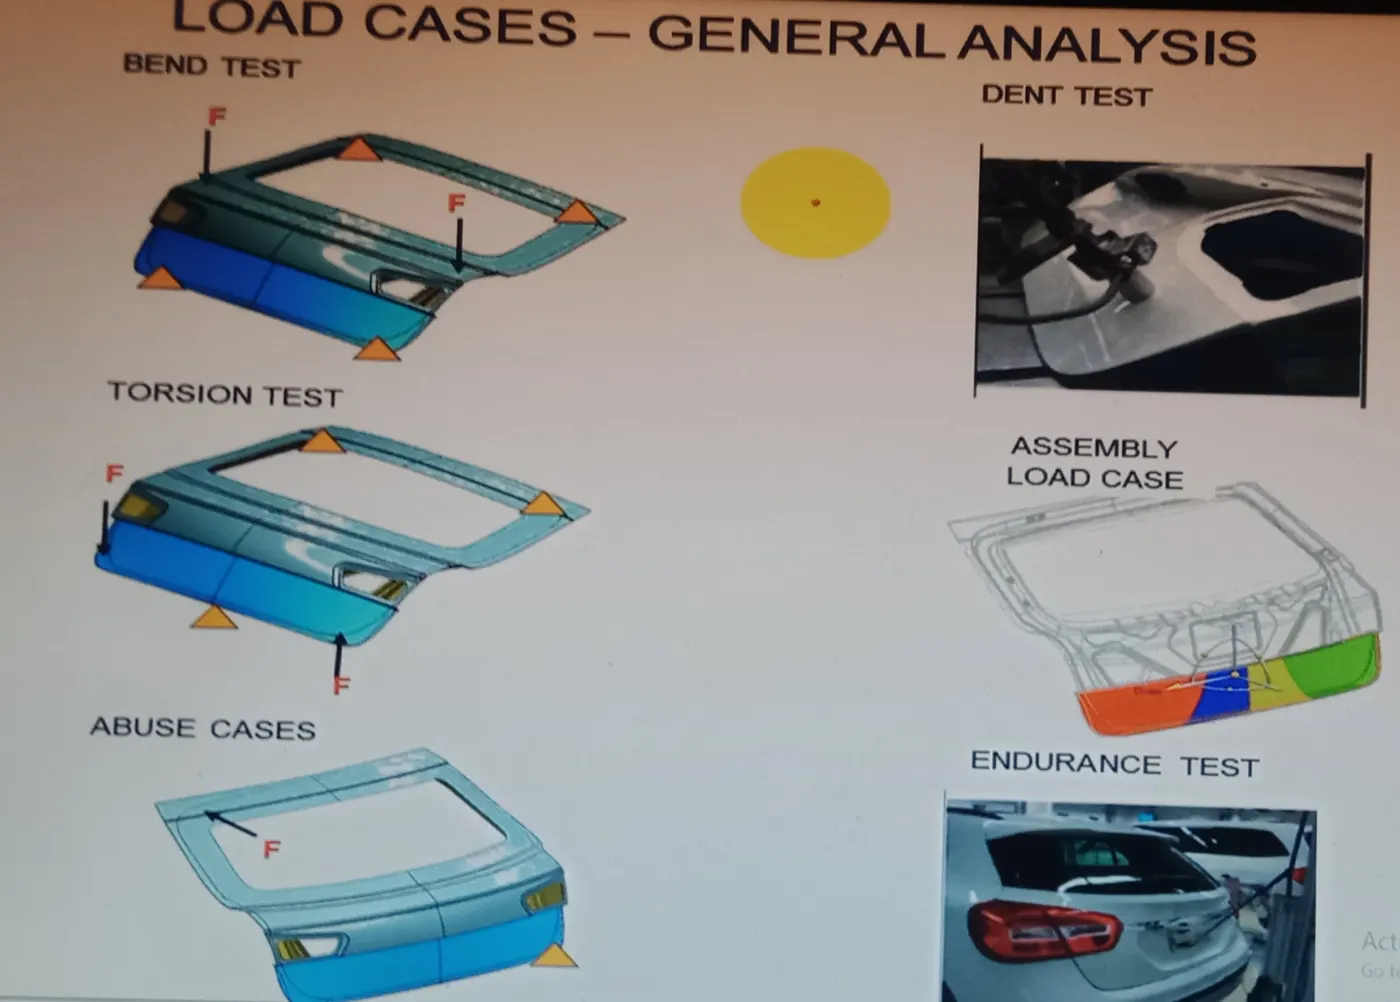
There are some tests done to ensure the strength of the tail gate which are
- Bend Test
- Torsion test
- Abuse Test
- Dent Test
- Assembly Load Case
- Endurance Test
Hemming :-
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts.
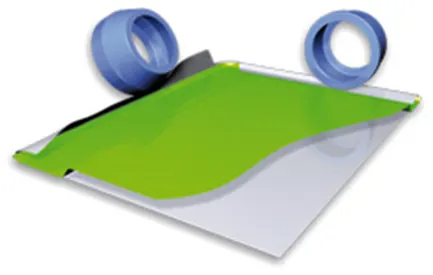 Roll hemming is carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller which follows a defined path.
In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
We join Back door Inner Pannel and back door Outer Pannel by this hemming operation. We create multiple flanges in Hood Inner Pannel. Top Flange of Hood Inner Pannel Becomes the part of this hemming process. The hemming edge of Backdoor outer panel after bending exceeds towards center of hood and overlaps the Hood Inner Panel flange till some length. Reliefs are also created at corners of flange. Definite gap needs to be achieved between the edges.
Hemming and Mastic Sealants combinedly reduces the need of spot welds between the hood inner and outer panels. Spot welds does not give aesthetic appearance to the car body while Mastic Sealants and Hemming serves this purpose greatly.