Design of backdoor
AIM:
Using the provided styling surface to come up with a back door and using appropriate design methodologies and make the necessary reinforcements and emboss.
Backdoor:
Backdoor is the part of a vehicle which is mounted on the rear side of a car. It helps in covering the luggage area with the help of sealant which keeps inside of the vehicle air tight and prevents water to enter into the car. The back door, sometimes referred to as the "Hatch," "Tailgate," "Trunk-lid," or "Boot-door," is a four-door car's fifth door. It's the region behind the last passenger seats generally. It has striker mounting as well as wiper motor mounts, tail lamps, and hinges to support the weight of the trunk when it is open, gas stays to help open and close the trunk, radars, cameras, and other features.
A Door is a hinged part which is used for entry and exit of the vehicles. Backdoor are one of the type of door of the vehicle which are located next to the passenger seat which provides access to the luggage compartment. In the most of the cars, these back door are operated with the help of gas stay which in turn reduces the effort required to lift the door. Some luxury cars have powered backdoor which in turn is driven by an electric motor. This kind of system is also called a powered trunk lid system hatchback or station wagons are sold as 3 doors or 5 doors models. In this case, the rear hatch is classified as door this is because it enters the passenger compartment. The naming is mainly used in Europe countries. In case of safety, the backdoor designed should meet the safety requirement of the rear collision.
Types of Backdoor based on working positions:
The door or opening of a cargo area may be hinged at the top, side & bottom. If the door hinged in the bottom it is called as a tail-gate.
1.Top mounted
2.Side mounted doors
3.Bottom type
1.Top mounted:
This type of back doors is used in a station wagon, pickup trunk and some of the spot utility vehicles. Today's modern cars use top mounted tailgating system which are both powered and also gas stay supported. These top mounted tailgates provide greater rear visibility compared to side mounted or backdoor which have center pillars in it.
2.Side mounted door:
As the name signifies the side mounted doors are the one which is used in the van type MPVs, SUVs, pickup truck vehicles. These side mounted doors or barn doors are a lot easier compare to top mounted doors. These doors are generally smaller in size and can be easily accessed. These doors are more convenient for the goods handlers for long pipe and lengthy components where one door is kept open. These door also save accidental head impacts. It is a lot easier to load and unload items in the side mounted doors
3.Bottom type:
This bottom type type backdoor system are used in the car type such as car, pickup truck and some luxuary SUVs. These are the most convenient type of back door in which the bottom split is used as a support or even as a table for the tour going people.
Types based on Working Mechanism:
1.Gas Stays type.
2.Powered Lift system.
1.Gas Stay type:
Gas Stay type backdoor is an ideal and most commonly used tailgate mechanism from lower segment car to luxury car segment. The ideal components of tailgate consist of a hinge, door, gas stay and some rubber beadings for sealing of door.
2.Powered Lift System:
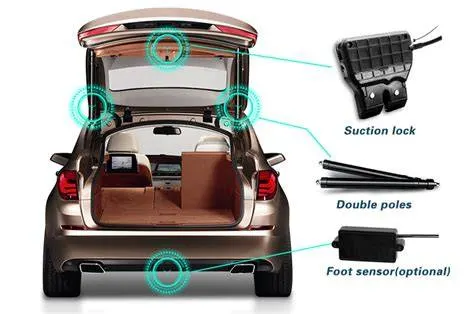
Power trunk lift system is another sophisticated way of trunk or liftgate opening mechanism which is to automatically open and close of the trunk and release of the latch by the touch of a bottom. Powered trunk Lift system consists of a power latch, anti pinch switch, PTG assly, PTG main switch. When the switch is pressed in the compartment or outside the power latch releases the latch and the entire backdoor is opened. The anti pinch switch is located in order to avoid accidental hand insertion during the operation of the door.also called electric tailgate or powertailgate.
Manufacturing methods:
Recently, there have been two approaches to reducing automobile weight. One is by using material lighter than steel and the other is by redesigning the steel structure. Althrough the former seems very effective, it is very expensive so that it may only be used for an expensive automobile industry is trying to use steel, which is not costly and recyclable. Light weight steel can be achieved by improving the performance of the structure or adopting by improving the performance of the structure or adopting new manufacturing techniques. One of the efforts is the ULSAB (Ultra Light Steel Auto Body) concept.ULSAB suggests three main weight reduction techniques such as hydro forming and the Tailor Welded Blank (TWB)
Tailor Welded Blank:
A Tailor Welded Blank is a blank that is compared of two seperate pieces of sheet metal that have been welded together prior to stamping. Tailor Welded Blanks allow the welding of the different grades, different thickness or different corrosion coating together in order to give the properties needed in differeent areas, without increasing the number of tools needed to form the part and eliminating the fit ability concerns. They also allow a high degree of flexibility in designing parts and large blanks can be formed from much smaller sheets. The use of Tailor Welded Blanks would reduce the weight of the car. Having the ability to selectively place different thickness of materrial would result in weight reductions. An example of this production is the door inner panel. The only strength requirement on a door inner is in the region where the hinges attach to the panel.
Different types of Sheetmetal operations are done in the Back Door
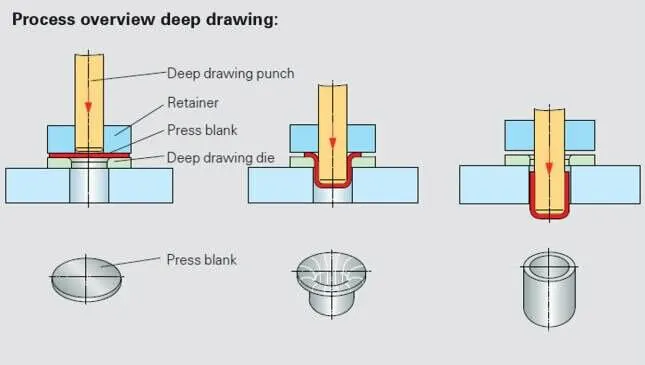
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
- First- stage drawing: The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
- Redrawing: The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
Embossing:
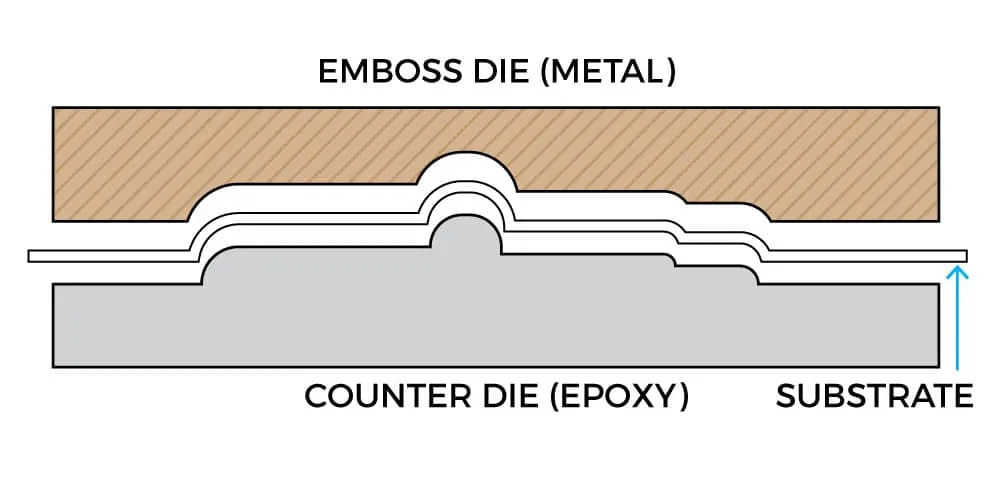
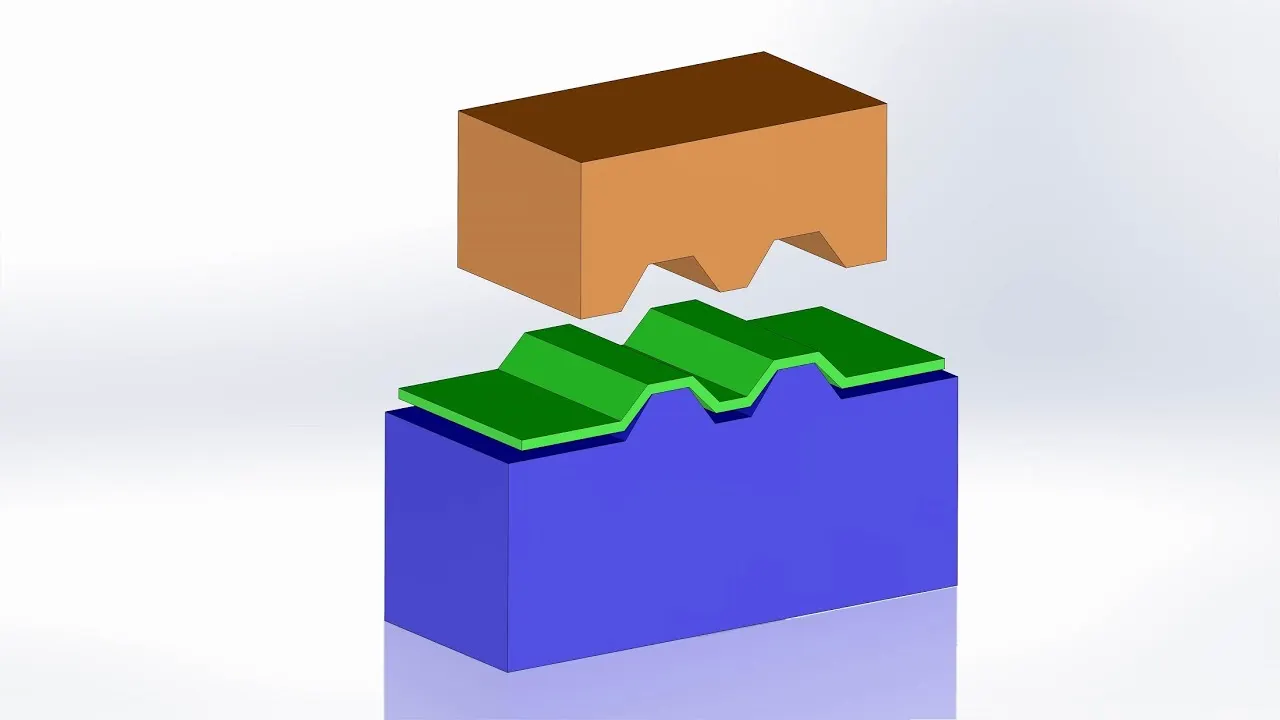
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
Hemming:
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
There are various types of hemming operations:
- Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
- Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
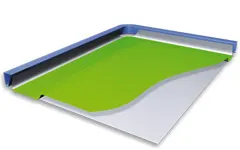
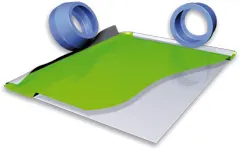
Open Hem: A Hem has a full round feature and a return flange. In open hem bend angle is equal to 180 degrees.
Tear drop Hem: In tear drop hem the bend angle is greater than 180 degrees.
Closed Hem: Hems without any inside radius are called as closed hem. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
Blanking:
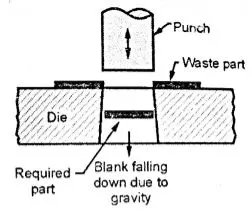
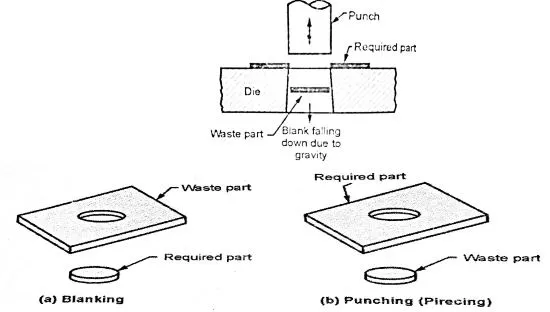
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered as a waste.
Punching:
It is similar to blanking only the main difference is that, the hole is the required product and the material punched out from the hole is considered as a waste.
so by using of aluminium we can reduce the number of parts and assembly involvement. and it is costly material.mostly it is casted parts.
Design Considerations:
- Rear Visibility Criteria
- Crash requirements
- Amount of space needed
- Accessibility
- Backdoor opening style
- Mountings
- Latch and striker placement
- Wiper motor placement
- Hinge and gas stay placement
- Reinforcements
- Sealing criteria
- Crash requirements
- Clearances
- Reliefs
Design Constraints for Back Door
The constraints for back door design are
- Rear Visibility criteria: The driver should be able to see from his seat to the rear side of the car. The visibility is the first and foremost factor which is taken into consideration.
- Boot Space: The gap between inner and outer panel should be in such a way that, proper section modulus (The factor which controls the stiffness and strength of the Model ) is maintained while giving enough boot space volume inside the car.
- Rear crash regulation and requirements
- Sealing and its functions: To make inside of the rear side of the car, sealing is provided for air and water tight for which sealing flanges are also designed. The width of the sealing flange should be atleast 25mm after blending all its edges. Sealing flanges are connected to the connecting flange to the windshield
- Joining Techniques followed like Hemming, Spot Welding etc.,: Hemming is used at the edges of the panels for assembly. Mastic seals are provided where spot welding and hemming can't be done. A minimum 5mm depth for mastic is provided between inner and outer panel ideally.
- Manufacturing Technique: Stamping, punching, bending, forming etc. are used in back dor manufactuirng. But it also varies according to the material being used.
- GAP and FLUSHNESS Requirements
- Functional Requirements of
- HINGE
- GAS STAY / POWER LIFTER
Hinges are provided for easy opening and closing of the back door. Gas stays are used to hold the backdoor. And for these, mountings and reinforcements are provided on the backdoor.
Parts thickness used in current design:
Outer panel: 0.75mm
Inner panel: 0.75mm
Reinforcement: 0.75mm
The Different panels or regions are as follows:
1.Inner Panel.
2.Outer Upper Panel.
3.Outer Lower Panel.
Backdoor Assembly:
A backdoor is normally manufactured with 1 inner panel and 2 or 3 exterior panels that are hemmed and spot welded together as needed. Depending on the price range of the car, different materials are utilised for the backdoor. The bulk of inexpensive cars are made of steel since it is less expensive, and parts are stamped using moulds. Here, uniform thickness of the panels is maintained throughout.
However, in expensive cars, aluminium is used for the manufacturing of back door which is usually die cast. In such cases, reinforcements are not required and the vehicle is also light in weight. Varying thickness can also be achieved in case of aluminium body back doors.
1.Inner Panel
2.Outer Panel
3.Hinge Reniforcement.
4.Gas Stay Reniforcement.
5.Wiper Motor Reniforcement.
6.Latch and Striker Reniforcement.
When designing the backdoor, we will divide the whole designing process into multiple steps which enables us to seamlessly create different parts of the backdoor assembly
We are provided with the styling surface and we take a top bottom approach to integrate the whole assembly
1.Inner Panel:
The inner Panel is a component which is used for strengthening the door and it is one of the most important components on which all accessories are mounted like hinges, glass guide channel, mounted trim, latch etc..,
The manufacturing method which may be used for creating the
The inner panel includes the deep drawing process in which the whole blank is inserted into the mold and perfect drafting angle is provided to the part so that the inner panel can be ejected easily.
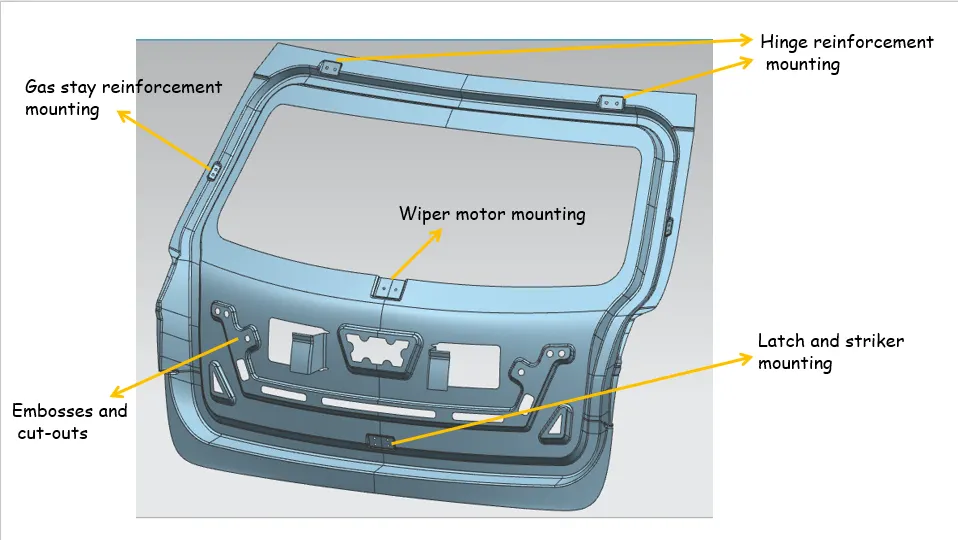
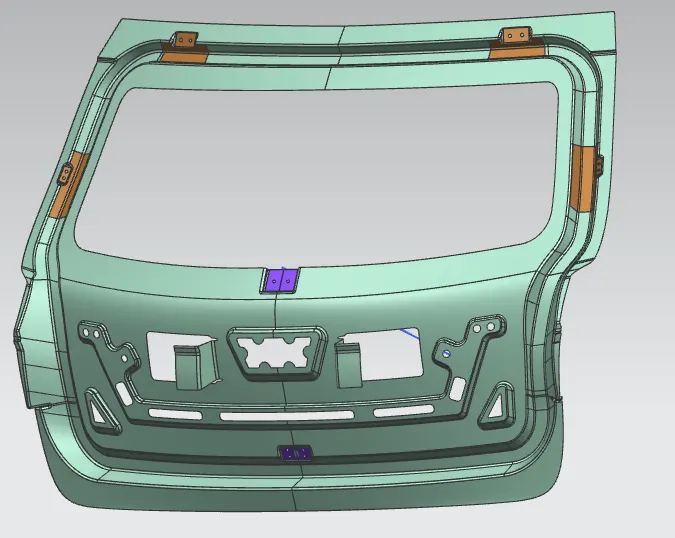
The inner panel is designed with embosses and several mounting for the Hinge , Gas-stay, wiper motor and Latch & striker surfaces.
2.Outer panel:
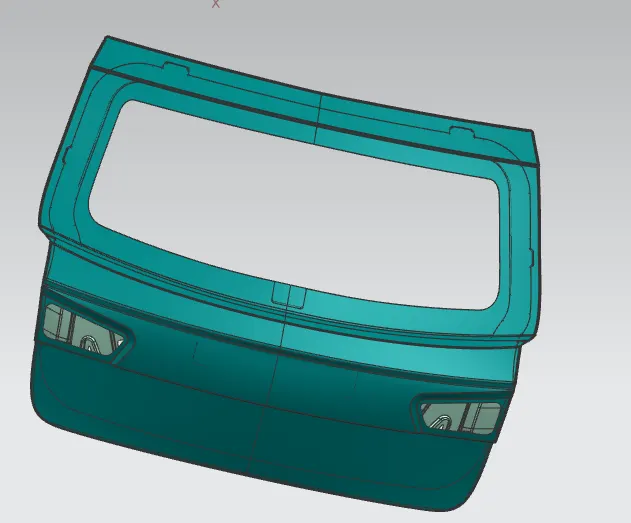
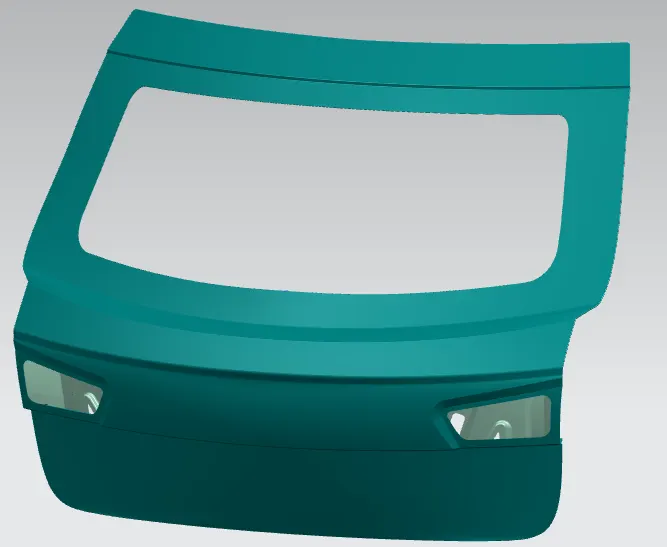
The Outer panel of the back door is similar to other BIW components where it is the aesthetic part of a vehicle. The coating provided is of multi stage which has the property of scratch resistance, rush prevention and smooth and attractive finishes. The Outer panel also has the provisions for the tail lamp, rear fog lamp and also has the provision for lisence plate mountings. Most of the hatch back cars have the provision for wiper motor.
The main purpose of reinforcements are to increase the strength of the part locally, since it is the place where the stress concentration would be great compared to other locations of the parts
3.Hinge Reinforcement:
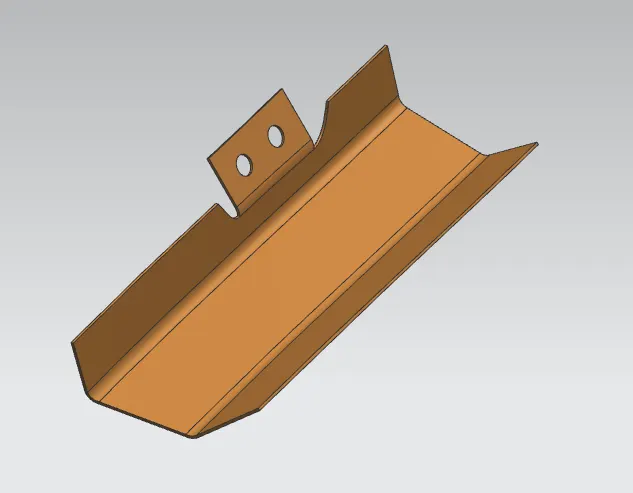
Hinges support the complete weight of the whole backdoor. Hence a hinfe mount reinforcement are provided here too. Embosses is designed such that the hinges should operated freely. The electrical wiring looms are through the holes along the periphery to keep them hidden.So the hinge reinforcements are made with sufficient strength to carry the loads
4.Gas stay Reinforcement:
An angled or Diabolic emboss is provided for the gas stay mounts. The angle makes it easy to be machined and stamped. It is reniforcement with a thicker sheet.
5.Wiper motor Reinforcement:
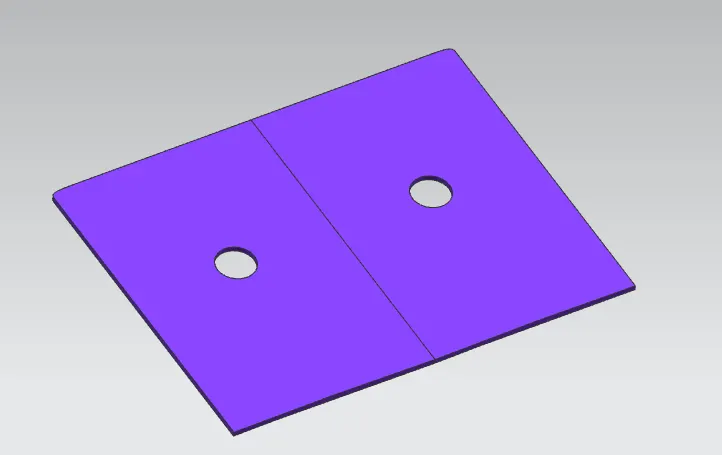
A dedicated space near the window is left for wiper motor assembly. A cavity is placed preferably in the middle of the panel to accommodate all the necessary wiper motor components
The holes or cavities are placed strategically to accommodate wiring looms, tail lamp mount, and other accessories. Embosses help stiffening the panel and act like local reinforcements. Extensions are provided around holes which are attached to outer panels and acts are crumple zone elements in case of rear impacts.
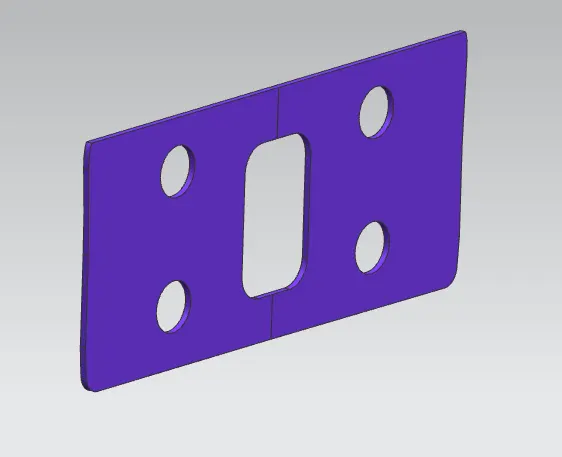
6.Latch and striker Reinforcement:
At the bottom of the latch and striker assembly. Generally a key operated or automatic remotely controllable locking mechanism is used to keep the door closed and open.
Another purpose of the emboss design is to distribute impact force towards hinges and latch assembly which are reinforced and can absorb them.
Components to create:
- Outer Upper Panel.
- Outer Lower Panel.
- Inner Panel.
- Gas Stay Reinforcement LH And RH.
- Hinge Reinforcement LH and RH.
- Striker Reinforcement.
- Wiper Reinforcement.
PROCEDURE:
1. Checking the Geometry:
- Once the model is opened, we get a Class A Surface of the back door.
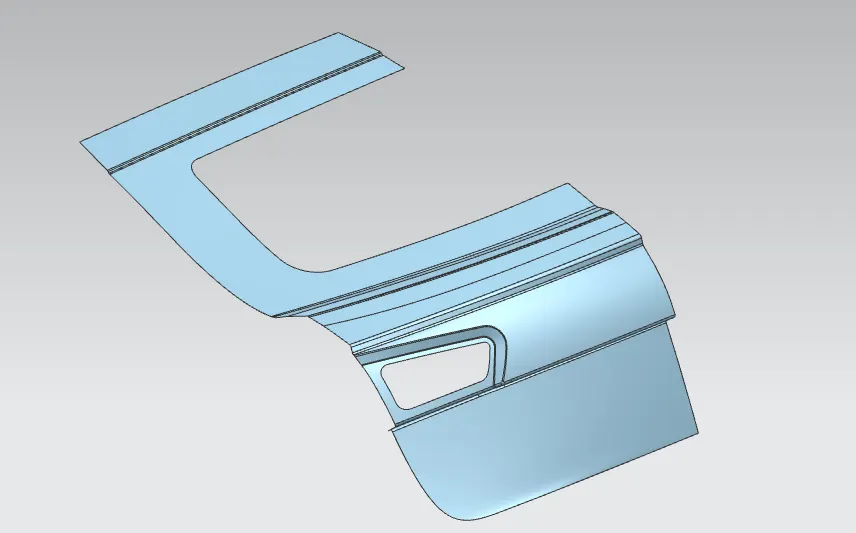
- Try joining the Upper surface of the car, if the surface sews together, we get the outer surface and if the surface didn’t join then we need to create the surface by using studio surface tool
- Create the fillet areas, Tail Lamp areas as those areas will be vulnerable and are unable to join together.
2. Tooling axis creation:
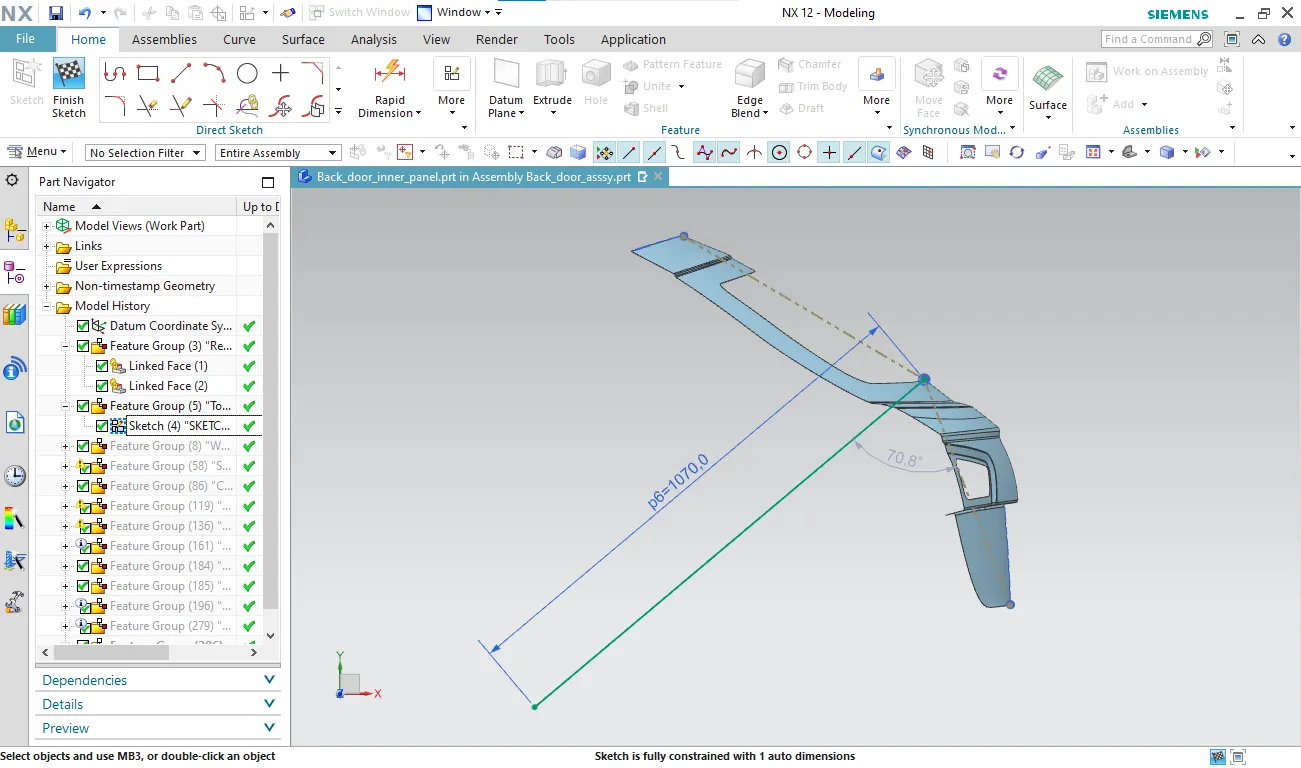
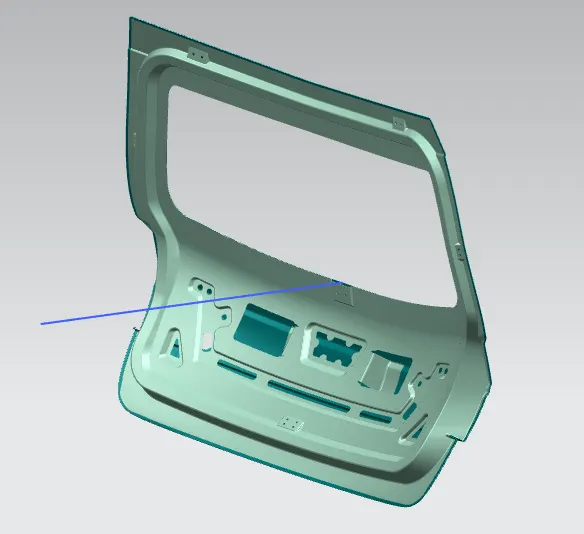
- Draw a line from left and right extremities almost parallel to the path of the surface along the unsymmetrical axis.
- Using the Derived lines tool, create a bsecting line as shown below:
3. Creating Inner panel
- First offset the surface to a distance of 1.7mm, which will give the innerpanel surface position.
- Now the sealing flange for the inner panel has to be created.
- The seaing flange created by cuttng from the surface is shown below:
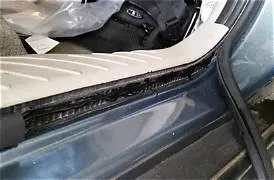
- sealing flange gets attached to weather strip(i.e, rubber sealant) which is 25mm width so we design sealing flange 30mm wide taking fillets into consideration.
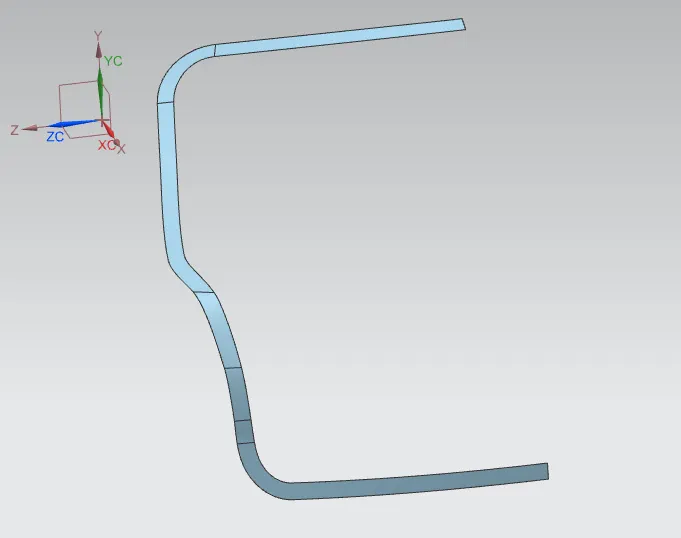
- In between, the tangent tensioning (Shape control) can be adjusted by modifying the surface using the Bridge curve tool.
- This flange has to be in a depth of 30 mm from the surface
- Now connect the flange with the surface using law extension w.r.t the tooling axis and proper draft given creating the connecting flange.
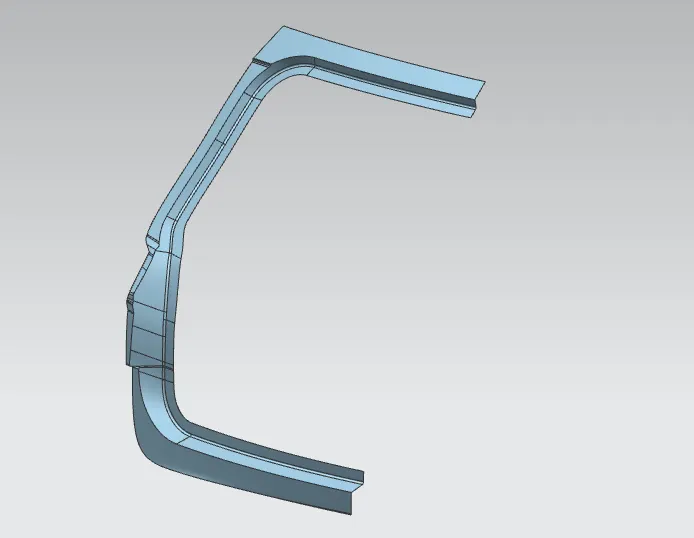
- Fillets has to be applied at each steps and check whether the surface is getting thickened or not.
- The next step is to create the other side which has to be connected with the sealing flange.
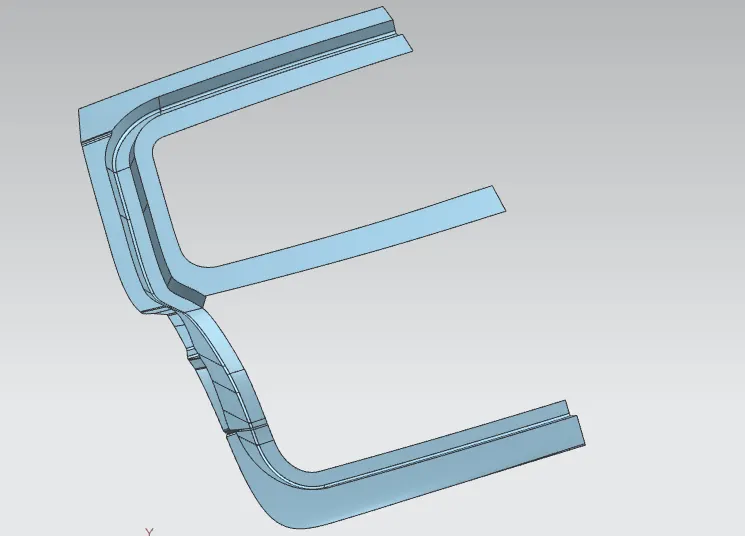
- Similarly connect the lower side of the surface by creating a surface and sew it all together.
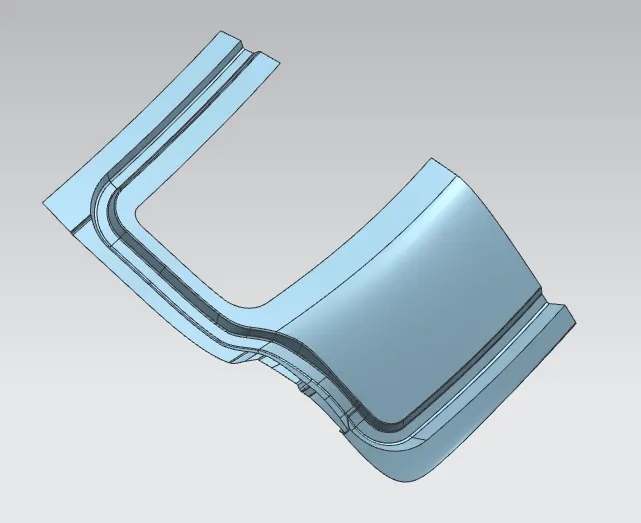
- A mastic sealent is used on the surface to connect the inner and outer panel with a gap of 5mm.
- Mastics are used for the purpose of joining one surface to another.here used to join backdoor inner panel with outer panel. It oozes out when heating and acts as sealing agent.
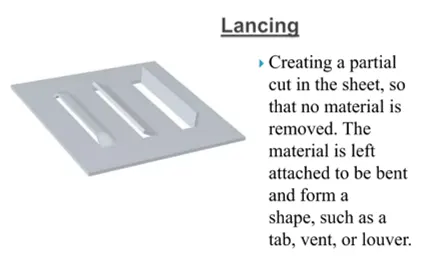
- we have designed mastic mounting region which is usually manufactured by two sheetmetal operation called lancing and bending.
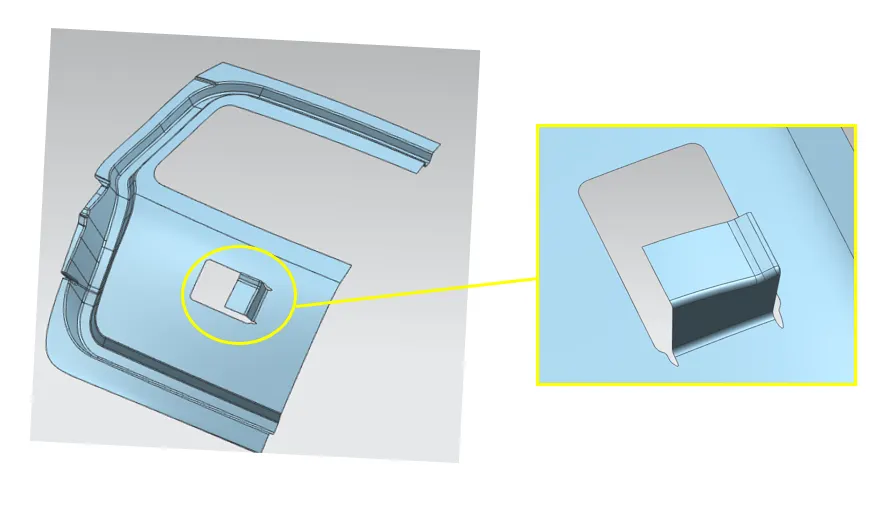
- So offset the outer surface 5mm downwards and create a plate from the inner panel.
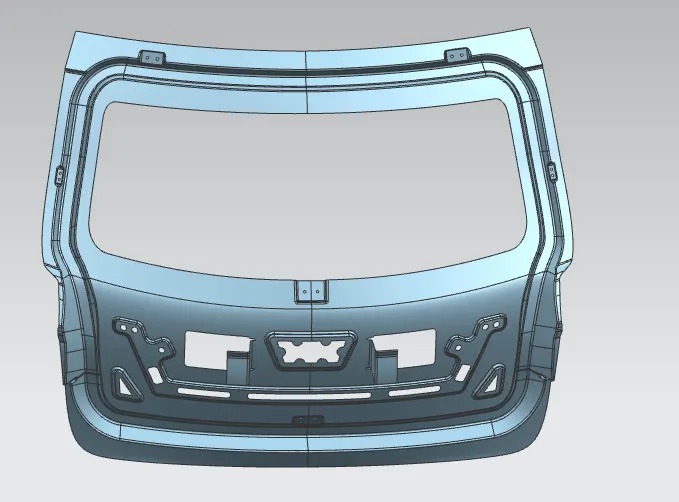
- Give proper embosses and cut-outs in the surface of the inner panel which is shown below.
- Now, embosses has to be created for the Hinge, Gas stay, Latch & striker as well as the wiper motor areas.
4. CREATING REINFORCEMENTS:
Hinge Reinforcements: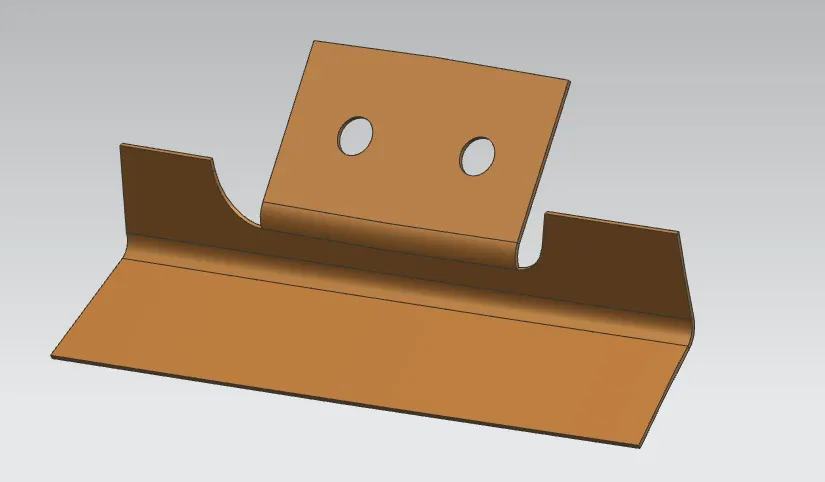 Gas Stay Reinforcements:
 Striker Reinforcement:
 Wiper Motor Reinforcement:
5. OUTER PANEL CREATION-UPPER :
- Offset the surface to a distance of 2.65mm so that 0.2mm of clearance can be given in between the surfaces.
- Later using law extension and three-face blend hemming surface is created.
- Closed hems , open hems are the most common type of hems where a sheet metal is connected to another part of the sheet metal using the sheet bending process alone without using welds or rivets. So that they can give very good surface finish.
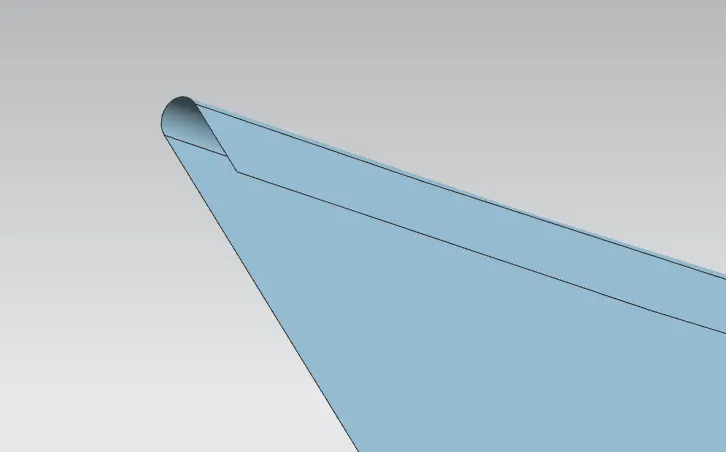
- Reliefs has to be given in the corner areas for the easy manufacturability.
- Hem reliefs are provided at corners to avoid stress concentration at corners having critical or sharp curvatures.
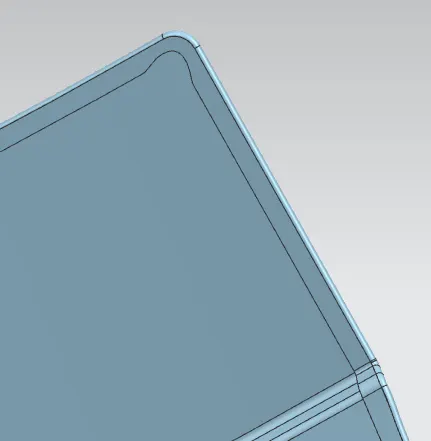
- The final part after creating the hem is shown below:
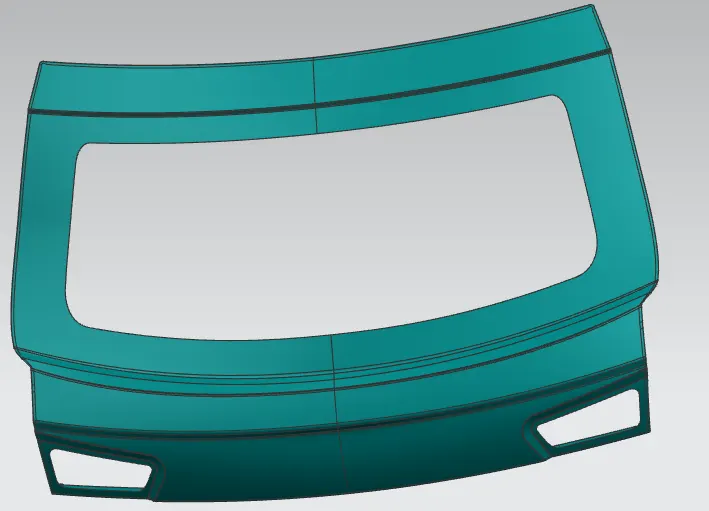
6. OUTER PANEL CREATION-LOWER :
- The same steps has to be followed for lower surface as well.
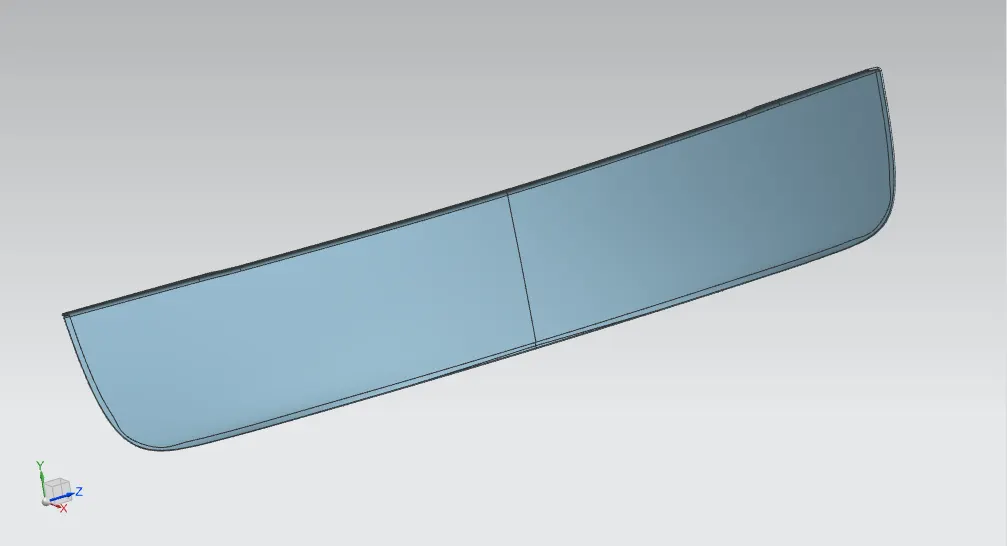
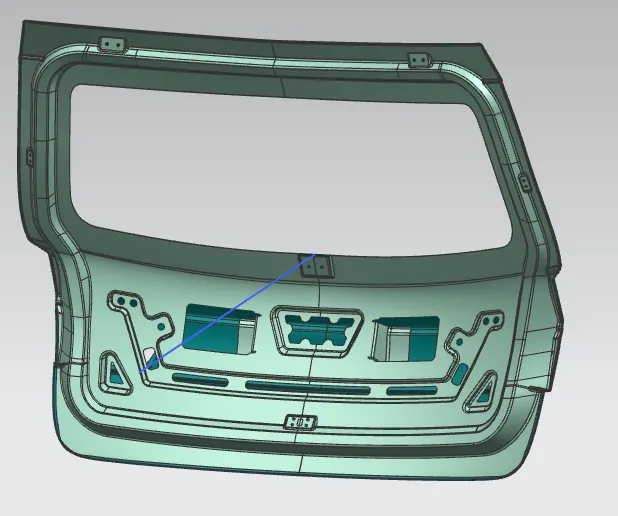
- The thickened part after the assembling of all these components is shown below:
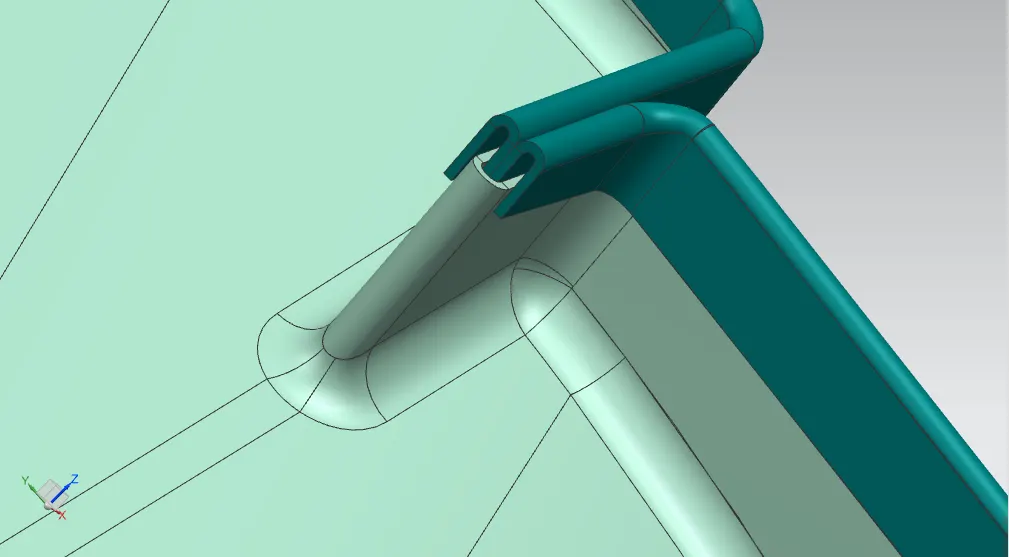 Back Door Assembly:
Tooling Direction:
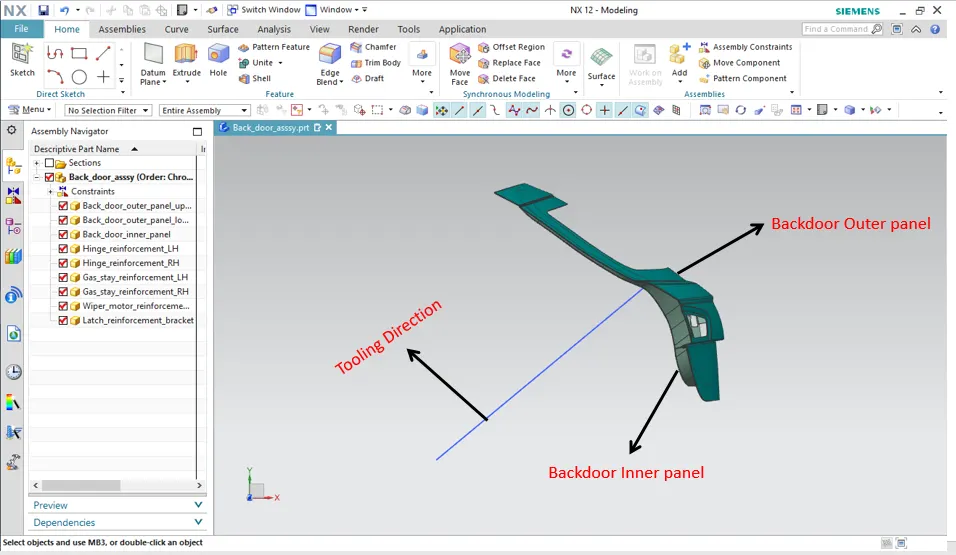
The direction in which the Core and Cavity open and close is known as the tooling axis. In order for the component to be easily ejected from the moulds, Design Engineers must analyse the Class A Surface and determine the appropriate tooling direction while keeping in mind that all drafting angles are with regard to the tooling axis.
The tolling direction is used as the reference vector to create all surfaces , embosses and draft angles. Because if we take a single vector as the reference to create all the surfaces, the tooling cost can be reduced and by just one deep drawing whole inner panel can be created.
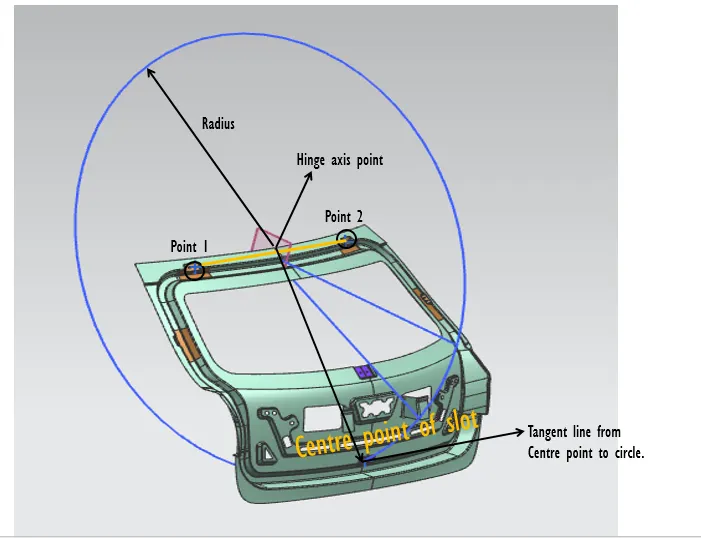
Trajectory for Latch and striker:
The radius between the hinge axis point and center of slot is used to trace the trajectory of the circle which can be used to locate the slot position on latch and striker reinforcement mounting.
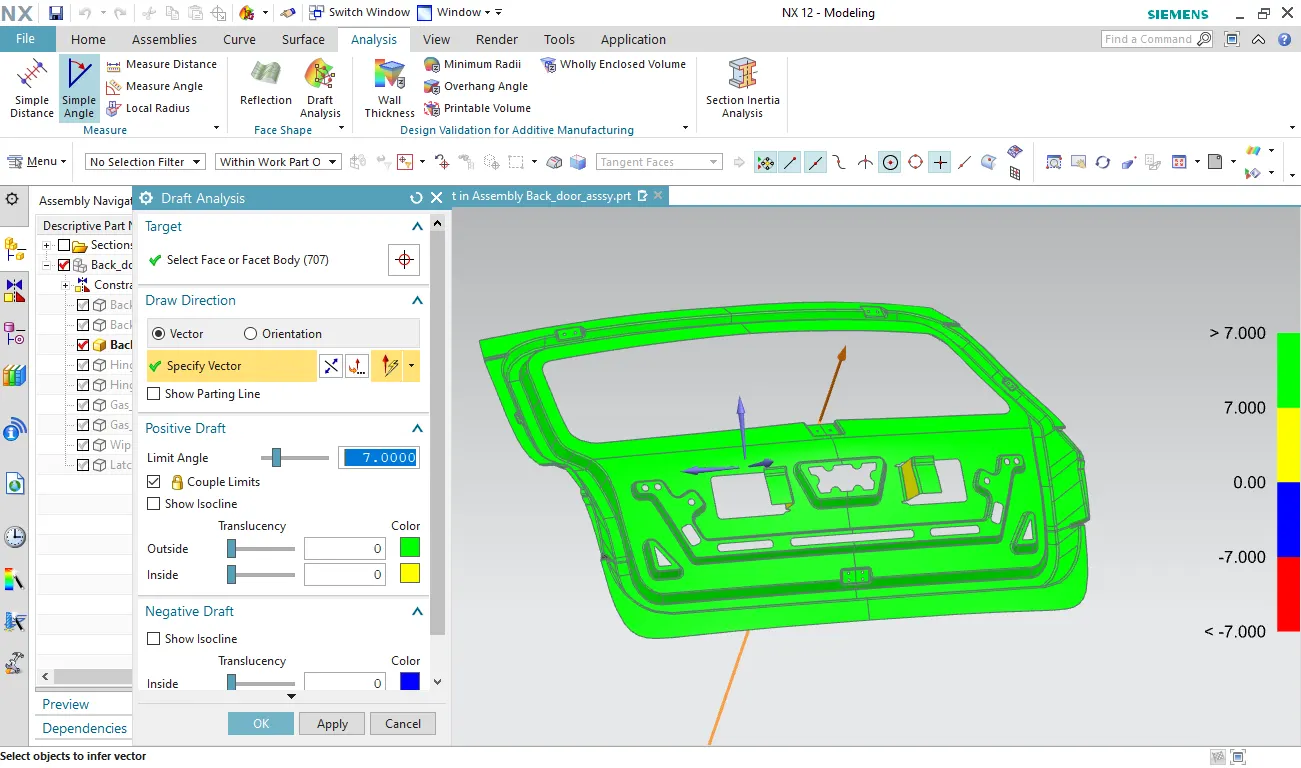
Draft Analysis:
Designers of plastic parts and mold tooling manufacturers can use the Draft Analysis tool to check the correct application of draft to the faces of their part. With draft analysis, you can verify draft angles, examine angle changes within a face, as well as locate parting lines, injection, and ejection surfaces in parts.
Draft analysis is done for the inner and the outer panel by taking the toooling direction as the reference vector.As per the sheet metal design considerations, almost 7 degrees is the minimum draft angle expected to ease the ejection of the part.
It can be seen all the parts pass the draft analysis successfully.
 Final Assembly:
Conclusion:
The sheet metal design principles are taken into consideration while designing the whole back door assembly using NX CAD successfully.