Design of backdoor
BACK DOOR DESIGN
OBJECTIVE
- To design the back door of a Car
- To design an inner panel for the back door.
- To design the necessary reinforcements like Hinge, Gas-stay, Wiper motor, Latch and Striker on basis of engineering standard
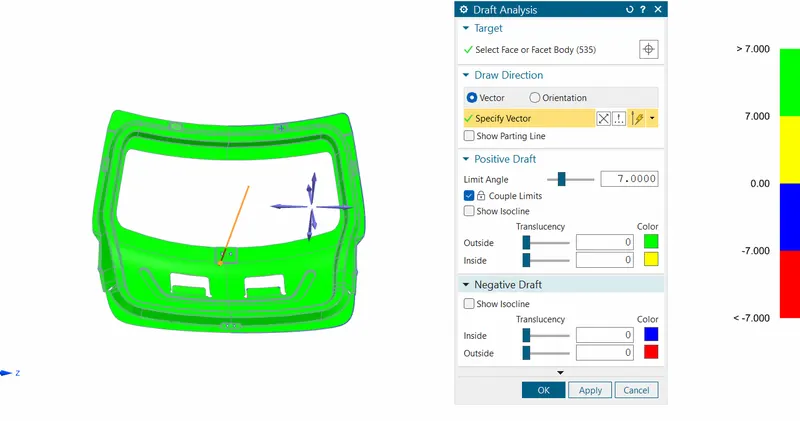
- The Inner panel is subjected to Draft Ana lysis for verifying whether it satisfies requirements of Deep Drawing.
INTRODUCTION
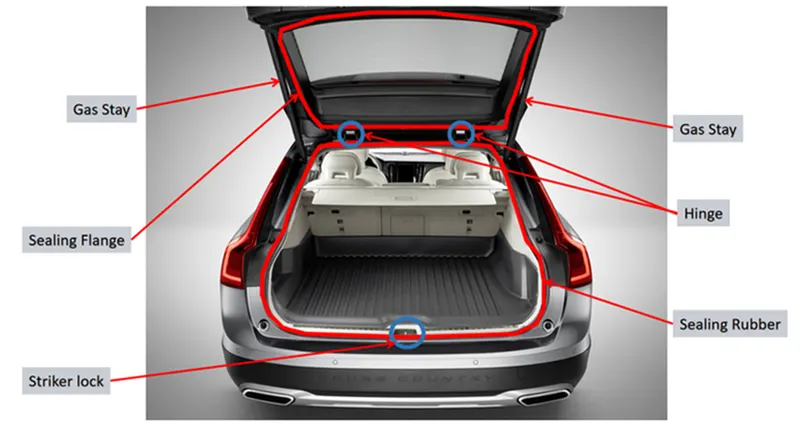
A door is a hinged part which is used for entry and exit of the vehicles. Back doors are one of the type doors of the vehicle which are located next to the passenger seat which provides access to the luggage compartment. In most of the cars, these back doors are operated with the help of gas stay which in turn reduces the effort required to lift open the door. Some luxury cars have powered backdoor which in turn is driven by an electric motor. This kind of system is also called a powered trunk lid system. Hatchback or station wagons are sold as 3 door or 5 door models. In this case, the rear hatch is classified as door this is because it enters the passenger compartment. The naming is mainly used in Europe countries. In case of safety, the back door designed should meet the safety requirement for the rear collision.
A backdoor is located at the rear end of the car which gives access for the boot space to store luggage, spare wheel etc. These doors cab be operated manually or electric powered. In most of the luxury car is electric powered. Back door is also called as 'Hatch' or 'tailgate', 'trunk-lid', 'boot-door' is basically the 5 door in a 4-door car. Its rearmost part of the vehicle which gives access to the trunk and has mounts wiper motor, tail lamps, hinges for supporting its weight in opened position, gas stay which help with its opening and keeping it open, radars and cameras etc.
A backdoor is usually made up of 1 inner panel and 2 or 3 outer panels joined together by hemming and spot welding wherever necessary. The material used for backdoor varies as per the price range of the vehicle. Most of the low cost vehicle use steel as it is cheaper and use parts are stamped using moulds. These parts are usually of uniform thickness and reinforcement are added to improve local strength where needed.
TYPES BASED ON WORKING MECHANISM
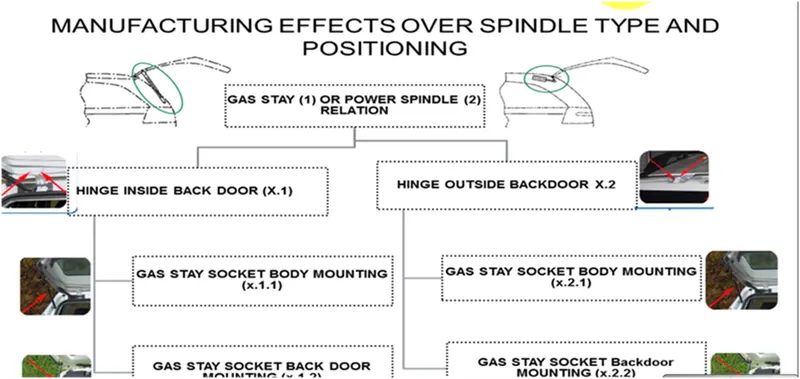
GAS STAY TYPE
Gas stay types backdoor/liftgate/tailgate is an ideal and most commonly used tailgate mechanism from lower segment car to luxury car segment. The ideal components of tailgate consist of a hinge, door, gas stay and some rubber beadings for sealing of door which is shown in the image below:
POWERED LIFT SYSTEM
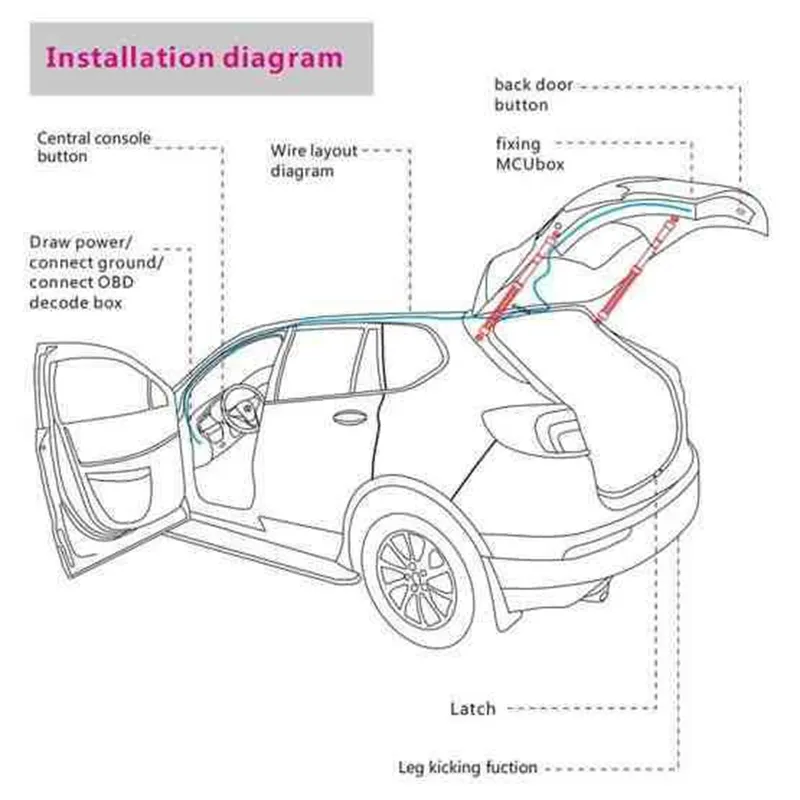
Power trunk lid system is another sophisticated way of trunk/liftgate opening mechanism which is to automatically open and close of the trunk/liftgate and release of the latch by the touch of a button. The following image shows the component as used in the powered trunk/back door lift system.
Powered trunk lift system consists of a power latch, anti-pinch switch, PTG assembly's, PTG main switch. When the switch is pressed in the compartment or outside the power latch releases the latch and the entire backdoor is
opened. The anti-pinch switch is located in order to avoid accidental hand insertion during the operation of the door.
MANUFACTURING METHODS
Recently, there have been two approaches to reducing automobile weight. One is by using material lighter than steel and the other is by redesigning the steel structure. Although the former seems very effective, it is very expensive so that it may only be used for an expensive automobile. Therefore, the automobile industry is trying to use steel, which
is not costly and recyclable. Lightweight steel can be achieved by improving the performance of the structure or adopting new manufacturing techniques. One of the efforts is the ULSAB (ultra-light steel auto body) concept.
ULSAB suggests three main weight reduction techniques such as hydro-forming and the tailor welded blank (TWB).
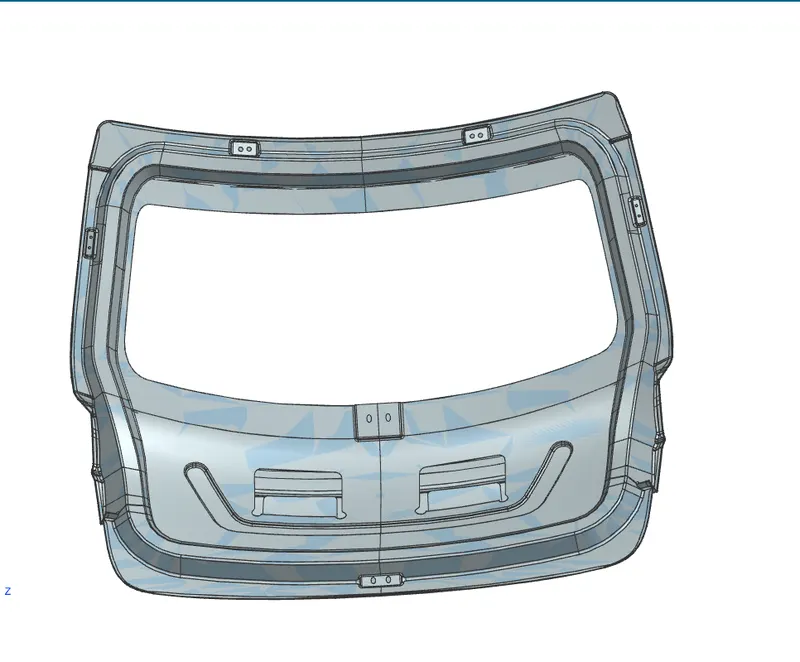
BACK DOOR ASSEMBLY:
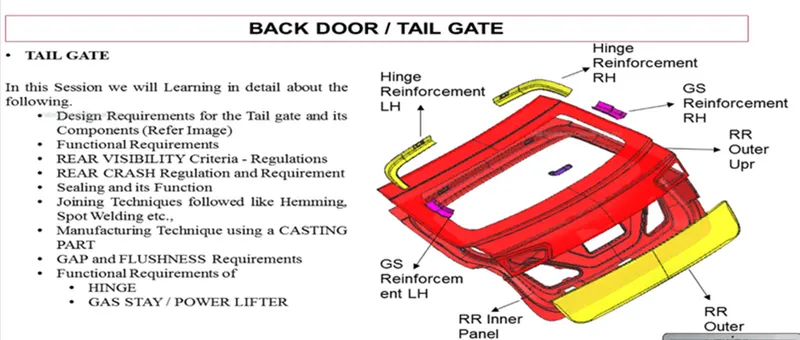
The back door assembly of a hatchback or SUVs has the following components.
- Inner panel
- Outer panel
- Hinge reinforcement
- Gas stay reinforcement
- Wiper motor reinforcement
- Latch/striker reinforcement
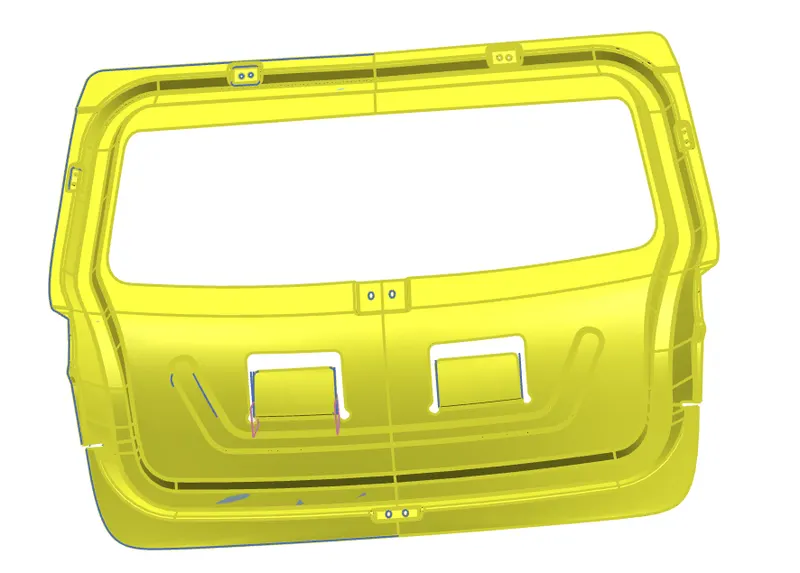
INNER PANEL:
The inner door panel is a component which is used for strengthening the door assembly and it is one of the most important components on which all accessories are mounted like hinges, glass guide channel, moulded trim, latch etc. The possible method is the integration method. In the integration method, the part is stamped out of a single blank. This reduces the number of tools needed; the assembly cost and eliminates any fit ability problem.
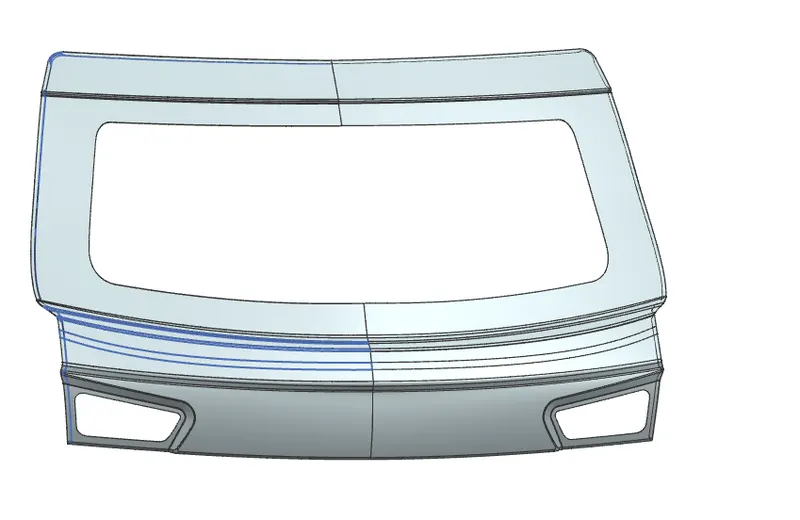
Outer panel:
The outer panel of the back door is similar to other BIW components where it is the aesthetic part of a vehicle. The coating provided is of multi-stage which has the property of scratch resistance, rust prevention and smooth and attractive finishes. The outer panel also has the provisions for the tail lamp, rear fog lamp and also has the provision for licence plate mountings. Most of the hatchback cars have the provision for wiper motor.
Back Door Assembly:
Draft Analysis:
The draft analysis command enables you to detect if the part you drafted will be easily removed. This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
Minimum draft angle of 7 degree is considered for analysis, green color infers on the parts that all face along the tooling direction has positive draft angle greater than 7 degree and passed in analysis.
Hemming Operation:
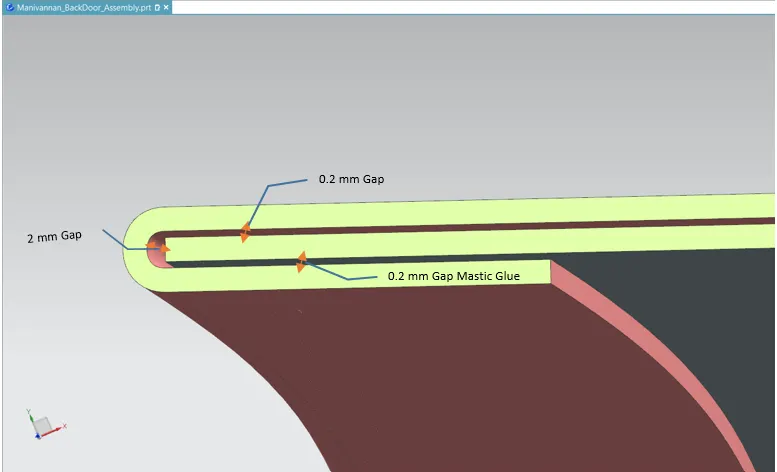
Hemming is a mechanical joints design which is used for joining inner and outer closure panels as found indoors, hoods, bonnets and lift gates. To increase crash resistance the gap between the hemmed panels is filled with a high strength adhesive which also prevents from corrosion.
Hemming Corner Relief:
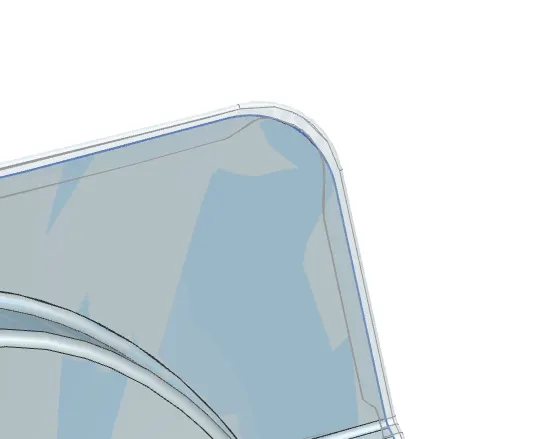
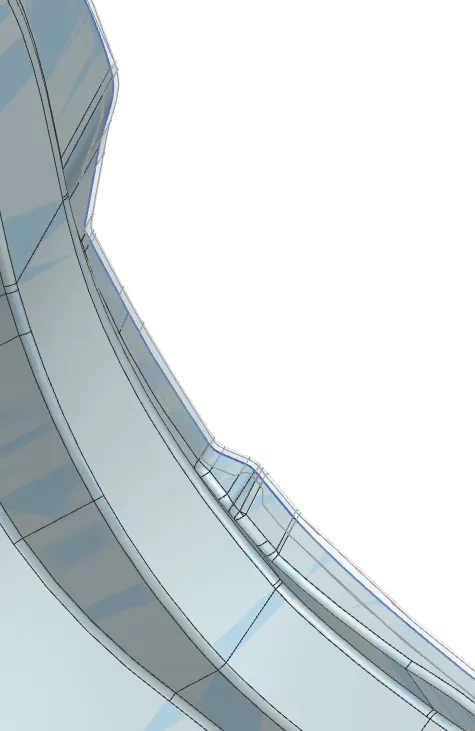
Hemming relief are cut out which are provided on the hemmed corner of the panel assembly which in turn to avoid some of the hemming defects such as wave – like or wrinkle formed surface as shown below,
The back door design requires two locations where the roller type of hemming relief is required which are shown belief.
What Is Sheet Metal?
Sheet metal is one of the shapes and forms metal can be bought in. Sheet metal is any metal that has a thickness in between 0.5…6 millimetres.
There are other measurement units used to categorise metals by thickness, though.
Millimetres, Mils & Gauge
Foils, sheets and plates are pretty much the same, with the only difference being in thickness. Thickness is measured in 3 ways – millimetres, mils and gauges. While millimetre is a pretty straightforward unit, mils and gauges are only common in engineering and manufacturing.
One mil equals to a thousandth of an inch. As the British often use “mils” as a plural for millimetres, it can be a little confusing but the difference is important.
Gauge is another unit for measuring sheet metal thickness. Although official standards discourage the use of gauges, they are not all that rare. Gauge represents the thickness of a metal in relation to its weight per square foot. A higher gauge number means a smaller thickness. 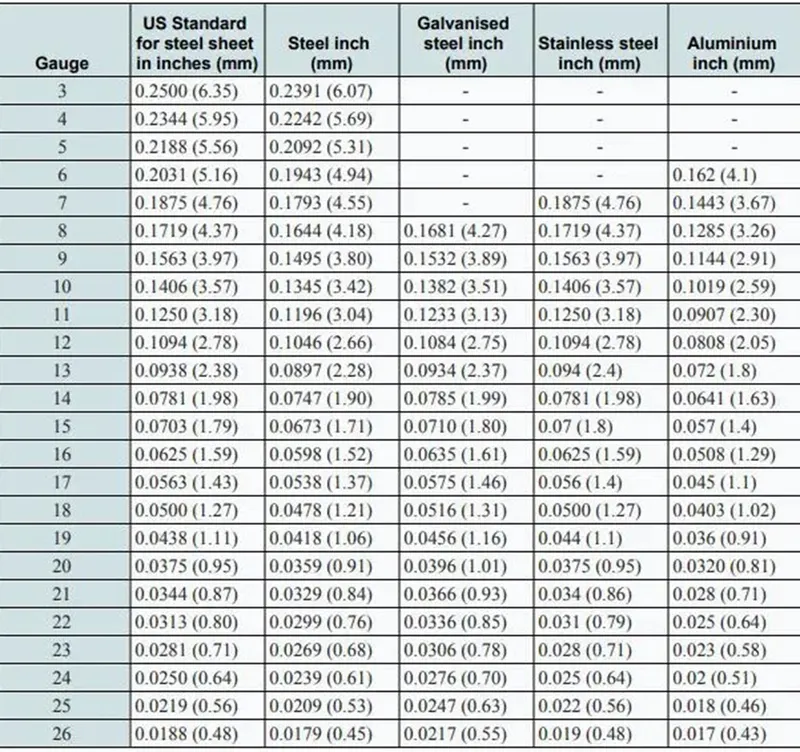
As it is related to the weight of a metal, the actual thickness (mm) for the same gauge, is different for various metals (e.g. 12 mm steel vs 12 mm aluminium).
Foil, Sheet and Plate
Having gone over the primary measurement systems, we can now look at the categorisation of foils, sheets and plates. For our purpose, we are going to stick with millimetres as the unit of measurement.
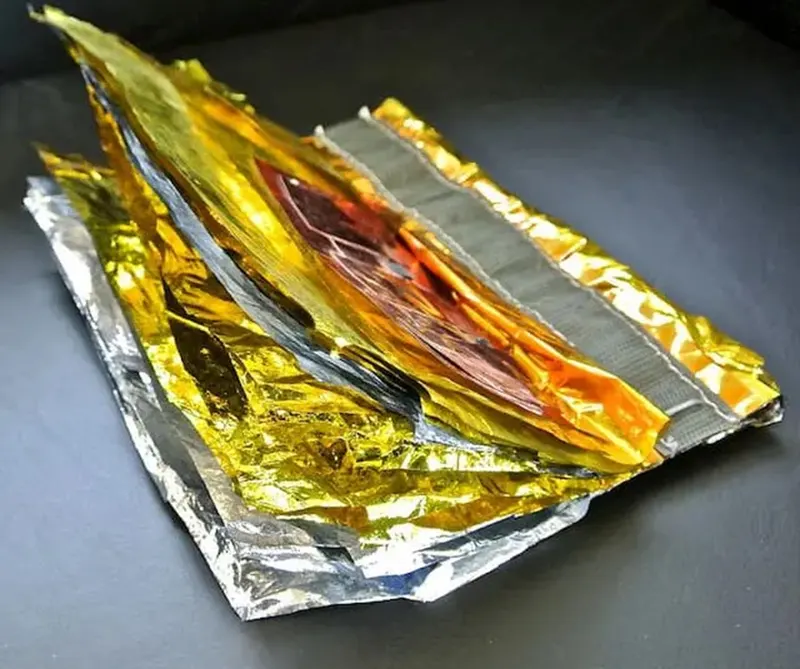
Metal foil :-
Metal foil is especially common with aluminium, often referred to as tinfoil. The thickness of foil is usually up to 0.2 mm.
Sheet metal is the next in line. The thickness of sheet metal starts from 0.5 mm and goes up to 6 mm. Anything above that is a metal plate.
The thin sheet metal is easy to form, while still providing great strength. At a relatively cheap price, it makes a great fit for most engineering purposes. That is why we see it everywhere around us.
At the end of the article, we will be discussing different forming methods used with sheet metal.
Common Materials :-
Pretty much all the common engineering metals are also used in the form of sheets. Some of them are carbon steel, stainless steel, copper and aluminium. Choosing the right one for you comes down to the application and requirements of your product.
Metal sheets have the same mechanical properties as the base metal. Thus, steel sheets have high tensile strength and durability suitable for use in constructions and machinery.
At the same time, copper sheets often find use as a decorative layer on modern buildings.
Standard Size :-
Standard measurements apply to both sheet sizes and thicknesses. While achieving large sheet sizes have a few workarounds through welding, you cannot really look past the thickness tables.
Standard Sheet Metal Measurements
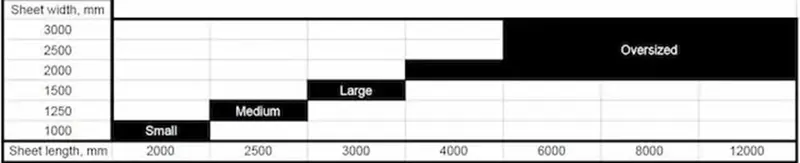
Knowing standard sheet sizes helps you with optimising your part layouts. Many times have we received parts for production that are just a bit larger than a standard size. That means more scrap and higher overall costs for the customer.
Also, another thing to bear in mind here is the availability of different sheet sizes. While small, medium and large sheets are pretty much always in stock at every sheet metal fabricator’s warehouse, oversized sheets may not be.
Many of them may also not have the machinery to cut such large sheets. So knowing your manufacturers’ capabilities comes in handy here.
Sometimes you can just weld together two smaller sheets but it is not the optimal solution. Especially when putting high emphasis on the aesthetics of your project.
Standard Sheet Metal Thickness
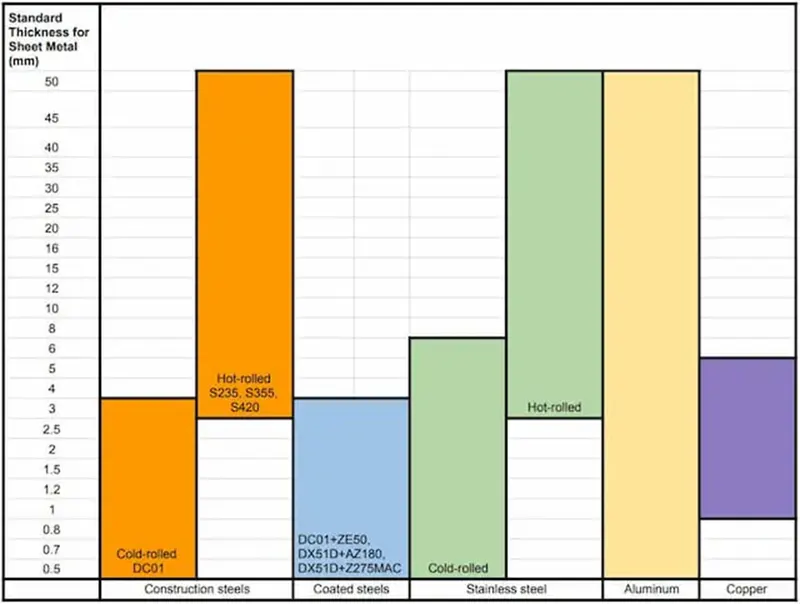
The table above shows standard thicknesses for both sheet metal and metal plates. As you can see, each type of metal has its own standards.
Also, it is good to not only pay attention to the starting and ending points but the actual values. Someone asking for non-standard thicknesses is quite frequent.
Exceptions to this table definitely exist. We would just advise you to follow these thicknesses because of the difficulty of finding the materials. All of the ones above are readily available with many sheet metal fabricators.
Get your manufacturing quote in seconds
- Quote in seconds
- Short lead times
- Delivery by Fractory
Hot-Rolled VS Cold Rolled Process.
There are two ways of producing sheet metal – hot rolling and cold rolling. Looking at the standard thickness table above, you can see how those two are used. In case of construction steels, cold rolling only goes up to 3 mm. From there on, the sheets and plates are hot rolled for cost-efficiency purposes.
Although the hot rolling process again starts from 3 mm for stainless steels, cold rolling covers all the sheets, i.e. up to 6 mm.
For engineering purposes, it is important to differentiate the two. For precision applications, cold rolled steels are preferred as we have more control over the final dimensions. This is because in hot rolled steels, after cooling, the steel shrinks slightly and the shape might change a little.
Forming Process For Sheet Metal.
So we finally made it to the forming methods for sheet metal. There is a plethora of options on the table and the decision rests on you.
The choice mostly depends on the required outcome. But many of those methods get you a seemingly similar or matching result. Then it comes down to cost (often depends on batch sizes), availability and desired accuracy.
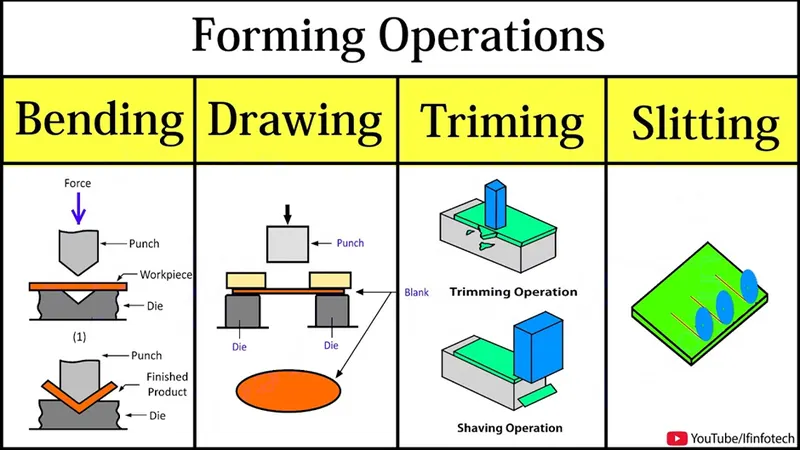
Sheet Metal Bending.
Bending is a forming process in which sheet metal is bent into the desired shape by applying bending stress. The sheet metal is bent so plastic deformation is reached. That prevents the metal from regaining its former shape.
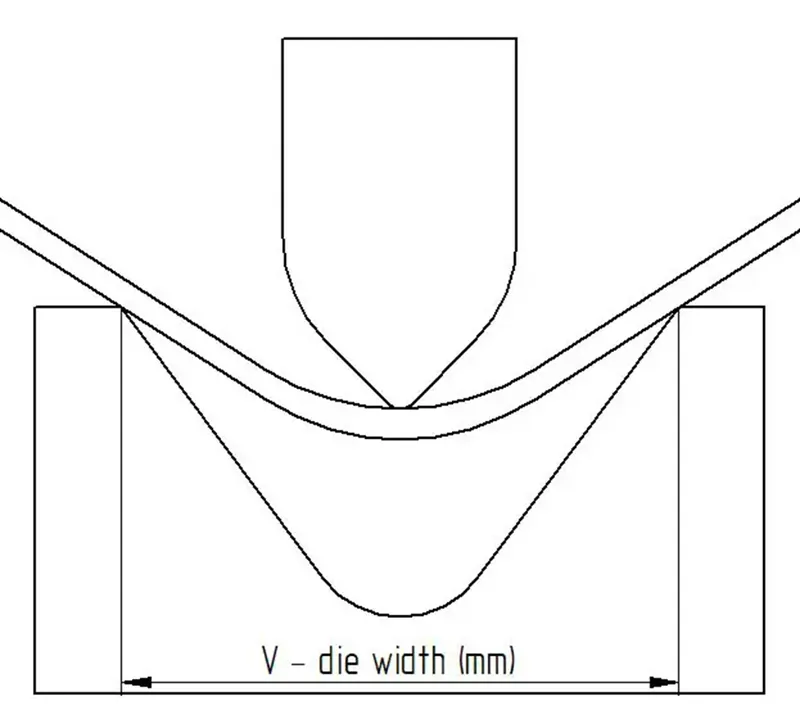
Air bending with a V-die
Parts such as flanges and corrugations are created by bending. The most common form of bending is V-bending. There, a V-shaped die and a punch press together to give the sheet the desired form.
Edge bending is another common method to bend flanges using a wiping die and a punch.
Sheet Metal Curling
Curling is the process of forming a circular ring at the edge of the metal sheet to make it safer for handling.
There is a difference between a curled edge and a tear-shaped hem. In curling, the initial edge is rolled into the formed circle whereas, in the tear-shaped hem, the initial edge is still exposed.
Curling can also be classified into an off-centre and an on-centre roll. Off-centre rolls have the centre above the level of the sheet, whereas on-centre rolls have the centre at the same level as that of the metal sheet.
Sheet Metal Decambering
Decambering is the process of removing camber from a sheet of metal. In a sheet of metal, especially in strip-shaped parts, a horizontal bend is produced when it is flattened into sheets.
In decambering, we remove this horizontal bend by flattening the edges to remove the camber. The force is applied on a deformed edge, and not on the face, to push it into a straight form. It is usually carried out on limited length sections.
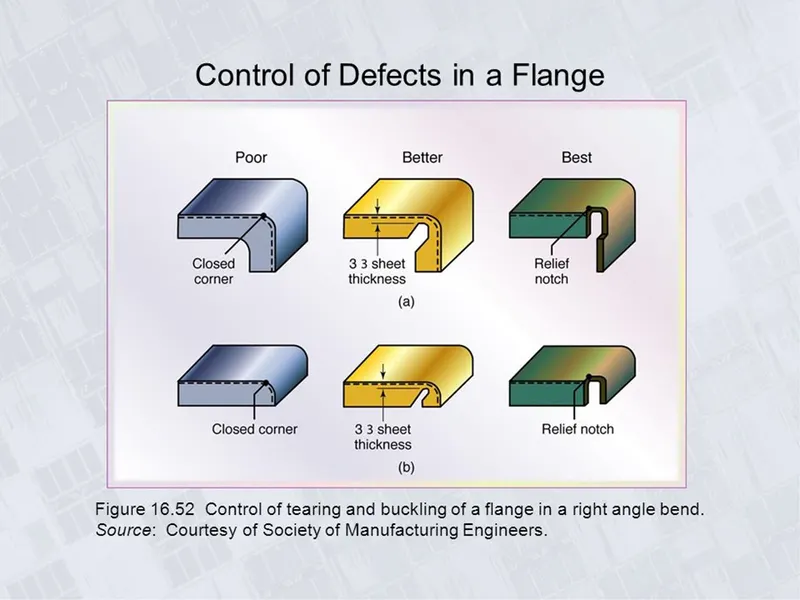
Deep Drawing
Deep drawing is a sheet metal forming process in which a sheet’s shape is changed to a desired shape in multiple stages using a series of dies. Only if the depth of the shape formed exceeds the original diameter of the sheet, it is considered deep drawing.
Punches and dies are used to create changes at every stage. Using this process, a sheet is converted into many different shapes like a fuel tank, sink, and automobile parts. Deep drawing is mostly used for large-batch production.
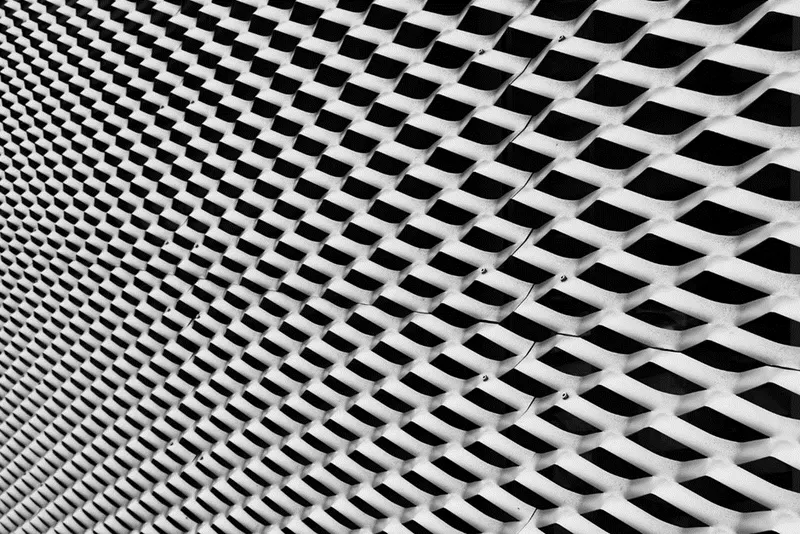
Sheet Metal Expanding
In this metal forming process, a sheet of metal is passed through perforating scissors where it is cut and stretched into a pattern. Usually, a diamond-shaped mesh is preferred as it has a structural advantage over other shapes.
This forming process is commonly used for manufacturing fences, catwalks, platforms, grating, etc. The process gives a self-draining, strong product that can support the weight it is designed for.
These products can be used where a passage of air or a liquid is needed but there is a need to prevent larger particles from passing, e.g. sifting. The strength of the original metal is retained.
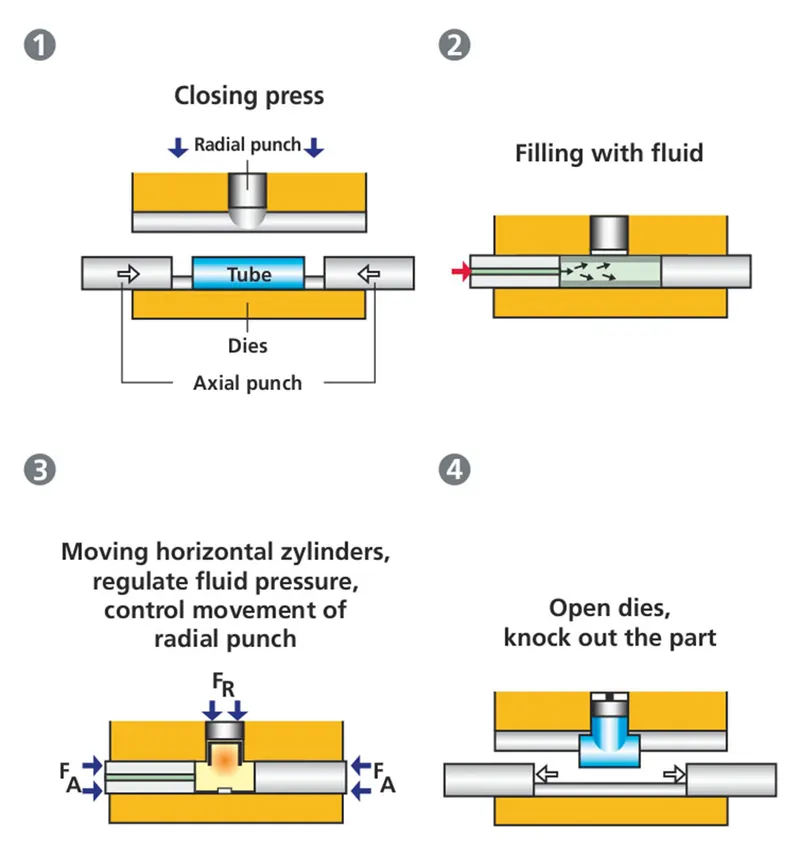
Hydroforming
Hydroforming is an innovative way of shaping metal sheets into a desired shape. In this process, the metal is placed on a die, but instead of a punch, high pressure fluid is used to shape the sheet.
With this process, more complex parts can be created in a shorter time-frame. It is also comparatively cheaper and requires less work. Hydroforming is also compatible with almost all materials such as stainless steel, aluminium, carbon steel, brass, and precious metals.
Since matching dies are generally not needed, hydroforming can be used to form unconventional shapes.
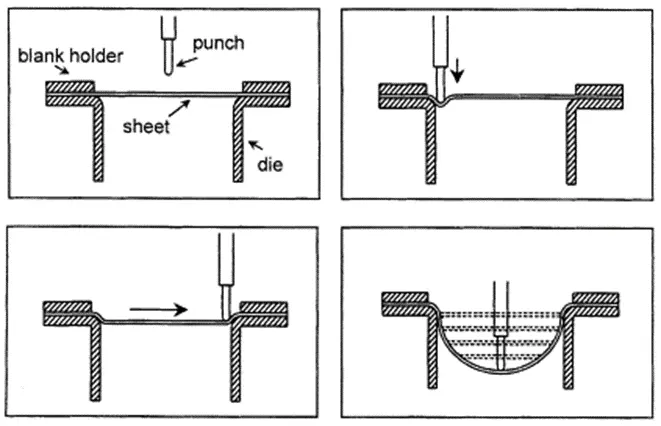
Incremental Sheet Forming
Incremental sheet forming is a metalworking process to give a sheet metal a certain shape. It is only viable with low volumes.
Changes can be made to the product quickly and without much hassle. In this process, the product is formed in incremental steps.
The sheet material is shaped using a single point sphere.
While the process gives a similar results to deep drawing, it does not need a separate set of punches and dies. So the largest advantage of this method is its flexibility.
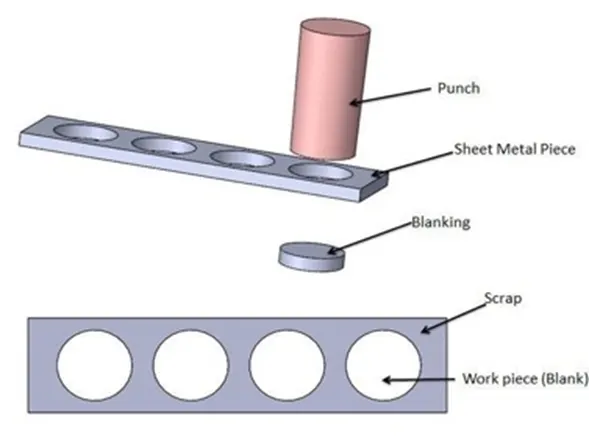
Punching
Punching is a very common technique for cutting holes in sheet metal. The setup consists of a punch and a punching die. There is a very small clearance between the two.
When the punch and the die meet, the material is pressed between the two and with subsequent pushing the shearing force cuts a hole in the sheet. The process is relatively inexpensive in large quantities and capable of punching a hole in strip as well as sheet metal.
Holes of varying sizes can be punched but it is usually recommended that the diameter of the hole required is greater than the thickness of the material being punched. For especially sturdy alloys, the difference between the hole diameter and the thickness needs to be greater.
Rolling
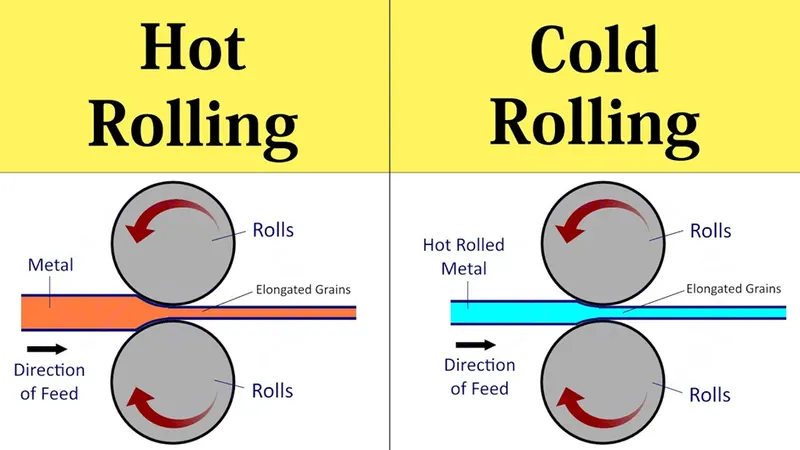
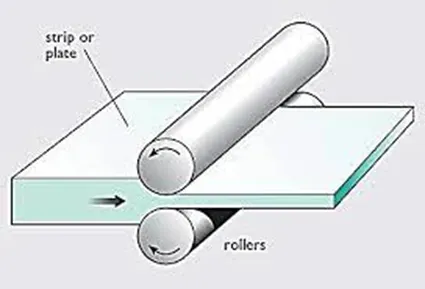
Rolling may be carried out on sheet metals to decrease overall thickness of the metal sheet or to make it more uniform. In this process, the sheet metal is passed through a set of rolls.
Depending on the temperature the process is classified as hot rolling or cold rolling. In hot rolling, the temperature is around 1400 degrees Fahrenheit for steel. This can help achieve a thickness from 1/16th of an inch to 5/16th of an inch.
In cold rolling, the process is carried out at room temperature. The material is washed with acid and heat treated to achieve a good finish.
Laser Cutting
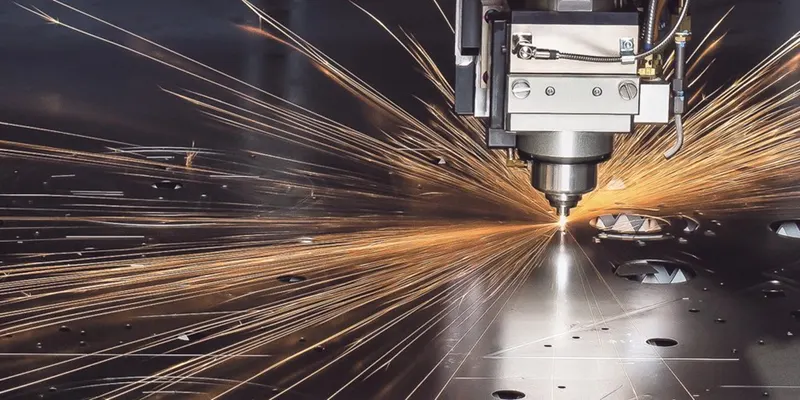
Laser cutting has become an increasingly common sheet metal forming process in recent years. With laser cutting, sheet metal is exposed to a high-powered laser that burns holes in the metal. It’s a faster and more precise cutting method that can even be performed automatically using a computer numerically controlled (CNC) laser cutting machine.
REINFORCEMENT:-
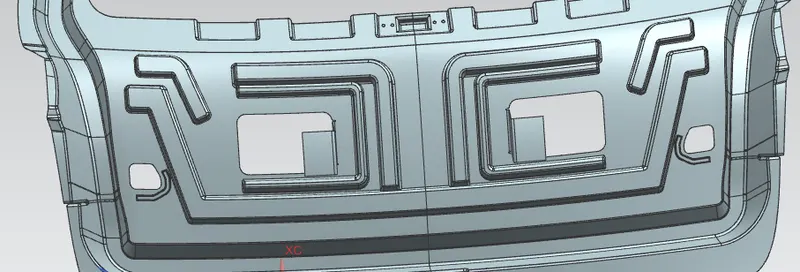
As mentioned for local strengthening reinforcement are usually provided. instead of making the whole panel off thicker sheet, a thinner sheet with thicker local reinforcements wherever needed is preferred. The reinforcement are usually 1- 1.5 mm thick whereas the panel itself is 0.55-1mm thick.
Embossing
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet material by means of matched male and female roller dies, theoretically with no change in metal thickness, or by passing sheet or a strip of metal between rolls of the desired pattern.
- Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
- Emboss should be in 7 degree to 25 degree inclinte in angle and it should not be in 90 degree angle,why because when we do stamping in manufacturing the stamping tool fits the sheet metal hence it will not come out of that sheet metal,So this is the main reason why the emboss face is in angle.
Characteristics of the metal embossing process include:
- Its ability to form ductile metals,
- Its use in medium to high production runs,
- The ability to maintain the same metal thickness before and after embossing,
- The ability to produce unlimited patterns, depending on the roll dies, and
- The ability to reproduce product with no variation.
- Located within the embossing stand itself are two engraved and mated hardened steel rolls, geared together to maintain top-to-bottom pattern registration. The width and diameter of these rolls depends on the strip width, material thickness, pattern depth, and material tensile strength and hardness.
- In most machines, the upper roll blocks are stationary, while the bottom roll blocks are movable. The pressure with which the bottom roll is raised is referred to as the tonnage capacity. This figure also depends on the aforementioned parameters.
- Embossing machines are generally sized to give 2" of strip clearance on each side of an engraved embossing roll. Many embossing machines are custom-manufactured, so there are no industry-standard widths. It is not uncommon to find embossing machines in operation producing patterns less than 6' wide all the way up to machines producing patterns 70"+ wide.
- The illustration that follows provides a two-dimensional look at a typical embossing line setup with an embossing roller in the middle. The illustration shows the metal sheet entering the roller, and then the embossed sheet leaving toward the drawing rollers.
-
Embossed metals are used in industry for two reasons: aesthetic and functional. Aesthetic applications also include appliance panels, building products, elevator panels, garage door panels, automotive trim, metal office furniture, and others.
- Functional applications are those in which a performance characteristic is enhanced. This can include a metal products ability to disperse liquid more effectively, reduction friction and static, increase a metal panel’s stiffness and rigidity, increase a metal surface area for acoustic or heat transfer applications, and improve traction.
- The embossing process can produce a variety of patterns. Some of the most common patterns include stucco, leather grain, wood grain, weather grain, and rough sawn cedar. Most embossers will tool to form any needed pattern, depending on the cost parameters involved.
Conclusion:
Thus,For the provided styling surface of a back door design, I used appropriate design methodologies and provided the necessary reinforcements and embosses for the BackDoor design.thus i designed a back door.