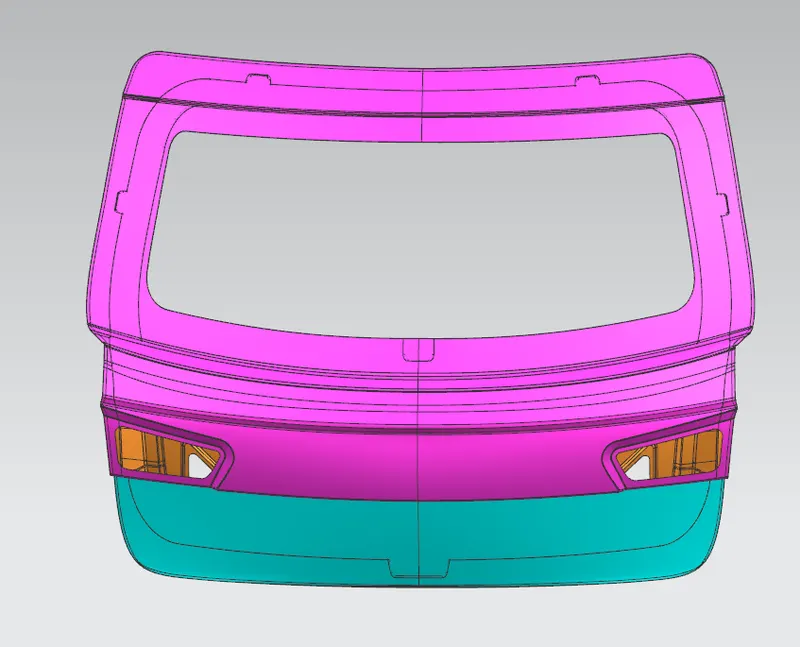
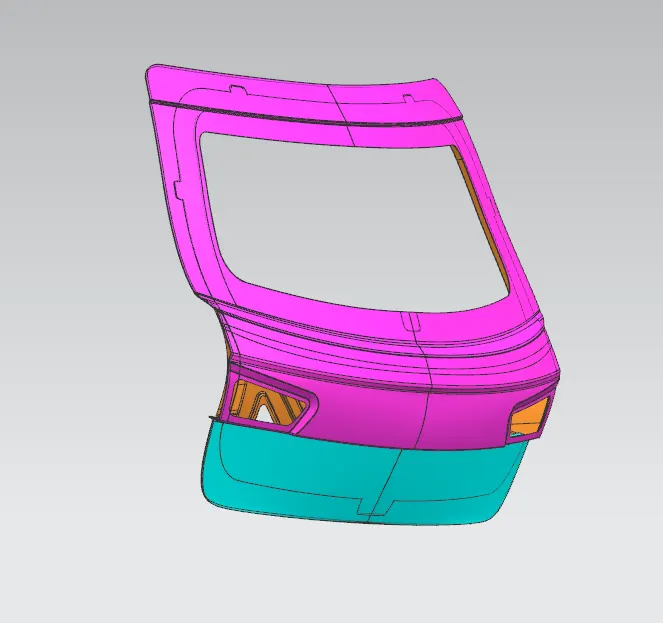
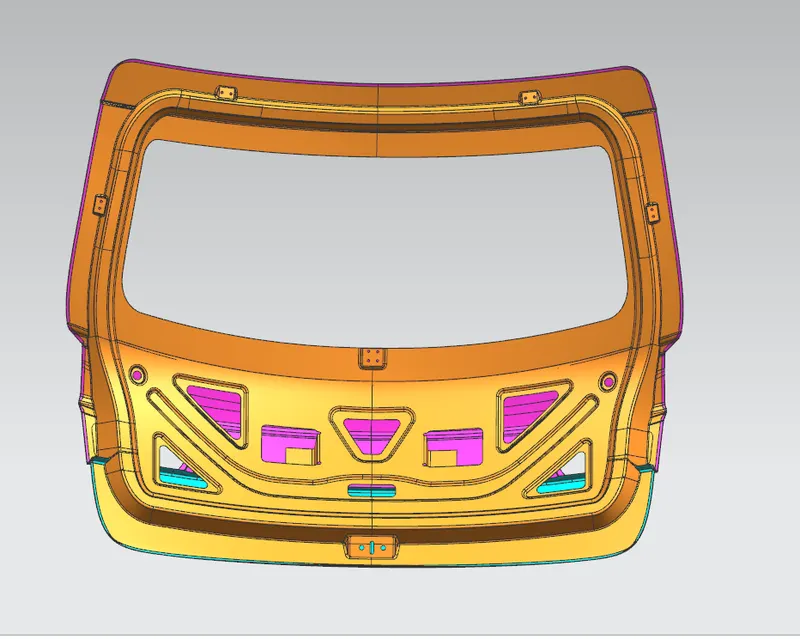
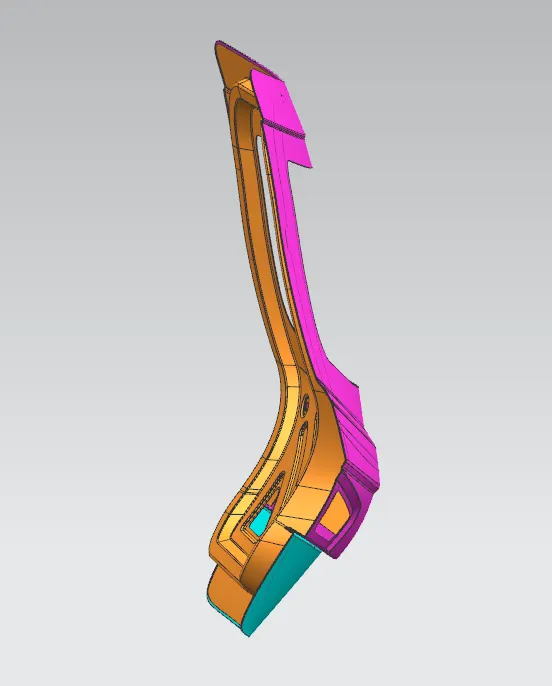
Design of backdoor
AUTOMOTIVE DESIGN OF CAR BACKDOOR USING UG-NX CAD
OBJECTIVES:-
- To develop a car backdoor using the provided class A surface with proper design methodologies.
- The objective of this project is to design a BIW Back Door of a car with an Inner Panel, Outer Panel, and Reinforcements for the Hinges, Gas stay, Wiper Motor, and Latch by following the engineering standards.
- The design should also pass the draft analysis along a tooling axis which is to be used in deep drawing.
INTRODUCTION
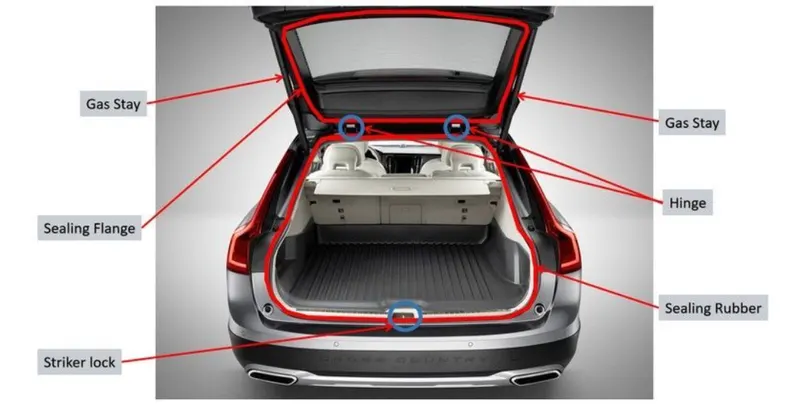
1.The Back Door of a car is the rearmost part of the vehicle which gives access to the trunk space of the vehicle. The rear door also supports the reinforcements and added weights of the Wiper Motor, Gas Stay, Tail Lamp, and Latch and Striker.
2.The design of the back door in body in white is done by keeping in mind the luggage space and rear visibility criteria.
3.Mostly the BIW of backdoor is made up of either steel or aluminum. The material used for door manufacturing depends on the budget and performance of the vehicle.Low-budget vehicles use Steel which makes the manufacturing process easy and cost-efficient since it follows the Stamping of Moulds.
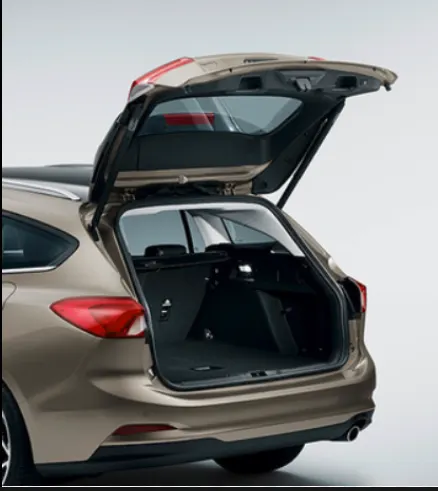
Major Parts and Reinforcements:
The backdoor consists of the following basic components:
1.Backdoor Outer Panel (Upper)
2.Backdoor Outer Panel (Lower)
3.Backdoor Inner Panel
4.Hinge Reinforcements (LH & RH)
5.Gas-Stay Reinforcements (LH & RH)
6.Latch and Striker Reinforcement
7.Wiper motor Reinforcement
TAILGATE
A tailgate is a door at the back of a truck or car, that is hinged at the bottom so that it opens downwards.
DESIGN INTENT
To develop the BIW car backdoor keeping in mind the design considerations which satisfy deep drawing,safety and cost effectiveness.
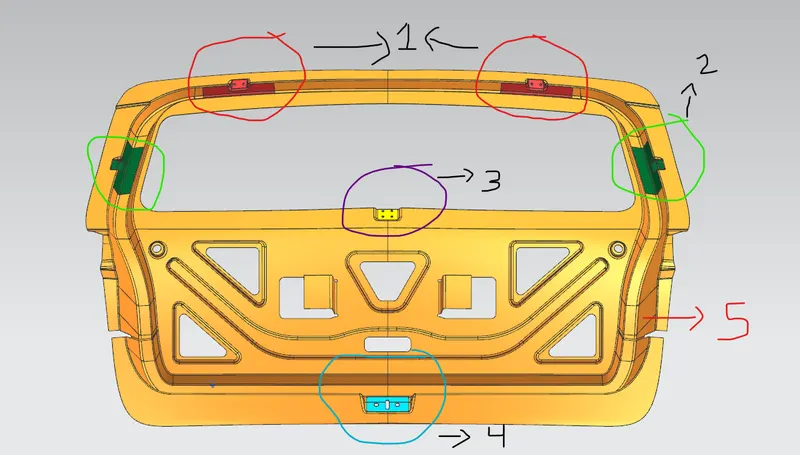
1.Hinge reinforcement
2.Gas stay reinforcement
3.Wiper Motor reinforcement
4.Latch and striker reinforcement
5.Backdoor inner panel
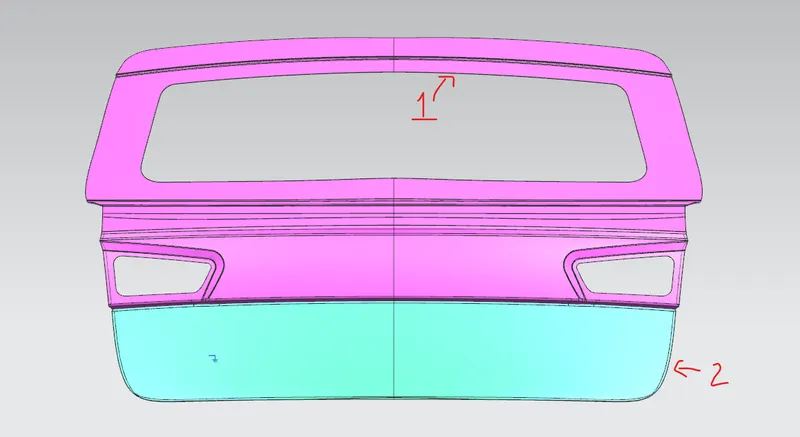
1.Outer panel upper
2.Outer panel lower
DESIGN CONSIDERATIONS
-
Functional Requirement of Hinge and gas stay
-
Rear visibility criteria
-
Luggage volume
-
Crash Analysis
-
Bend Test, Dent Test, Torsion Test & Endurance Test
-
Rear Crash Regulation
-
Gap and flushness Requirements
DESIGN OF BACKDOOR OUTER PANEL UPPER:
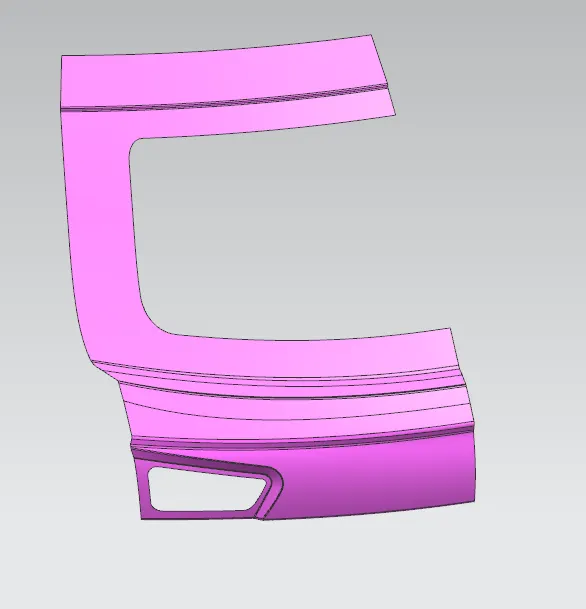
The provided class A surface was irregular ,so firstly repaired it using trimming and recreating the surface and sewing operations.
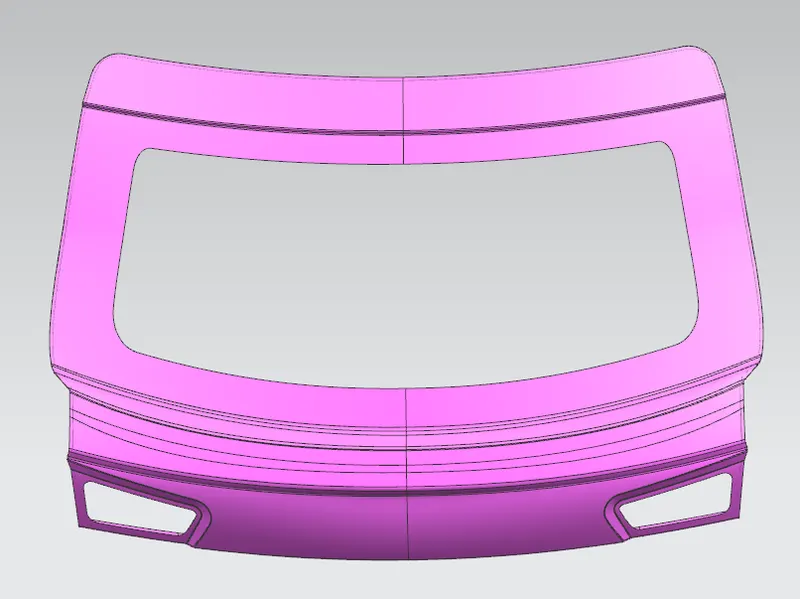
Later on mirrored the surface along y axis.for creating the hemming surface law extention was not providing the required results due to surface irregularities hence used sweep command in parts and later on sew them to make the hemming surface.
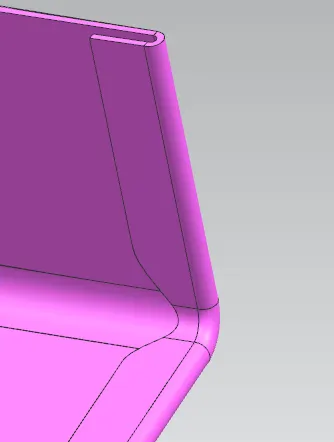
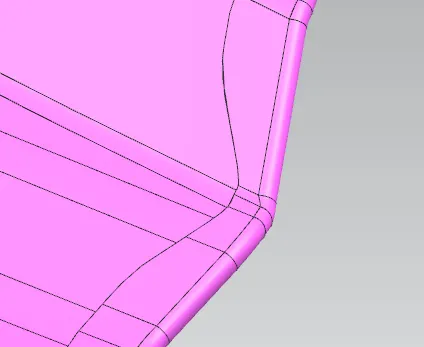
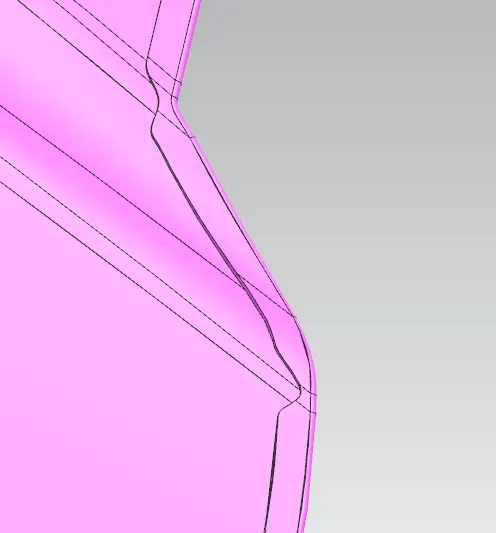
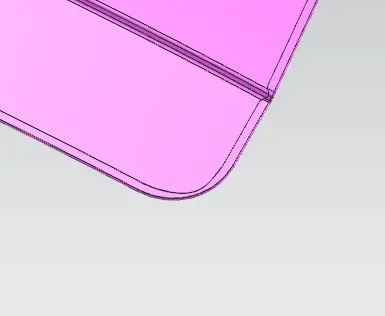
After mirroring ,made an extra sheet around the surface for hemming,provided a thickness of 0.75mm and provided corner reliefs.
DESIGN OF BACKDOOR OUTER PANEL LOWER:
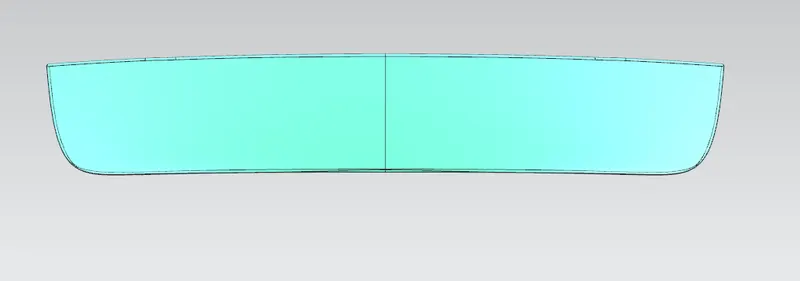
From the provided Class A surface ,mirrored it,made an extra extended sheet for hemming operations ,provided thickness of 0.75mm and corner reliefs.
Outer Upper & Lower Panel:
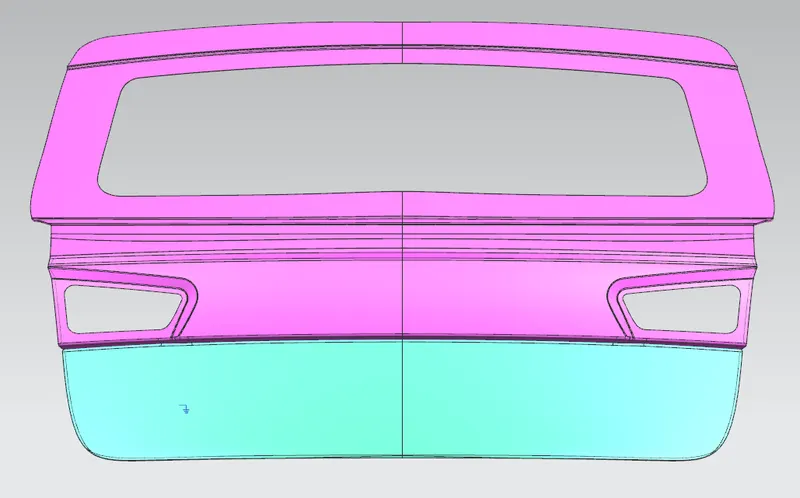
Tooling Direction:
- Before starting to work on the inner panel tooling axis is created by taking the bisection of two lines ,which is perpendicular to the surface so the this direction can be considered at the time of deep drawing by the production department.
- Also the provided class A surface of inner panel is checked and repaired for further designing.
- The designing approach is TOP DOWN APPROACH.Top down approach starts with the big picture, then breaks down from there into smaller segments.
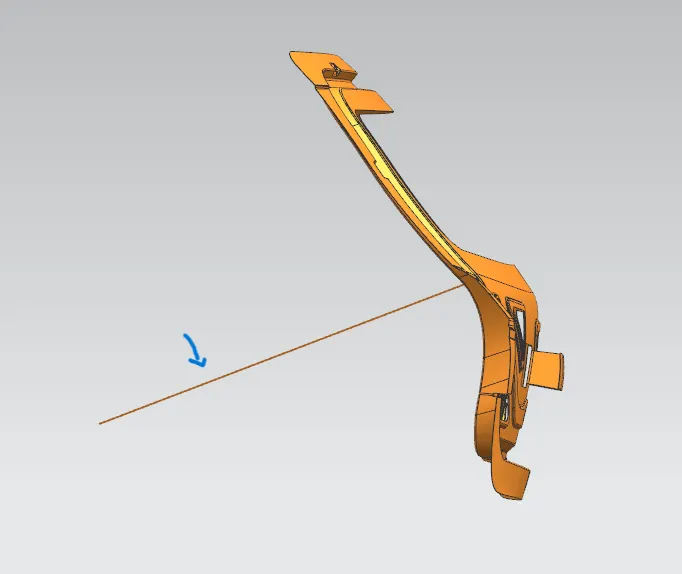
The blue arrow is showing the tooling axis .
DESIGN OF BACKDOOR INNER PANEL:
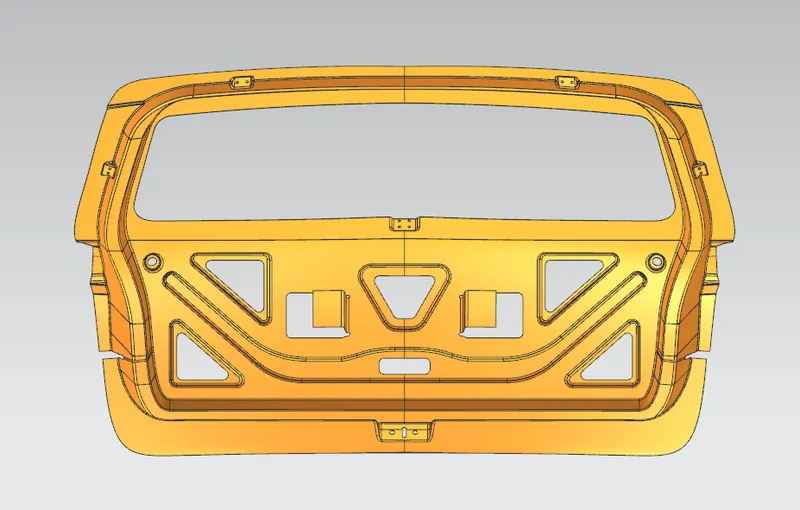
- Inner panel is extracted from the Styling surface.
- Checked and repaired according to the designing requirements.
- After this the development of SEALING FLANGE takes place.By creating multiple flanges and by using surface modeling techniques the concept design of the inner panel was created.
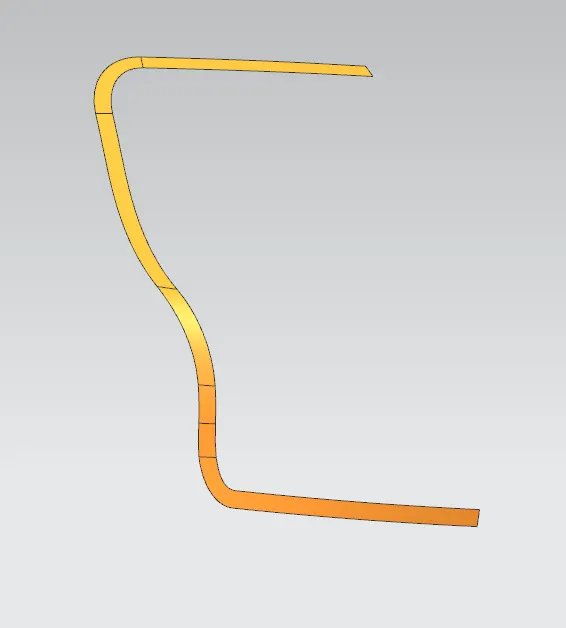
The sealing flange .
- Later by using Law extention and trimming and edge blends operations the inner panel is developed.
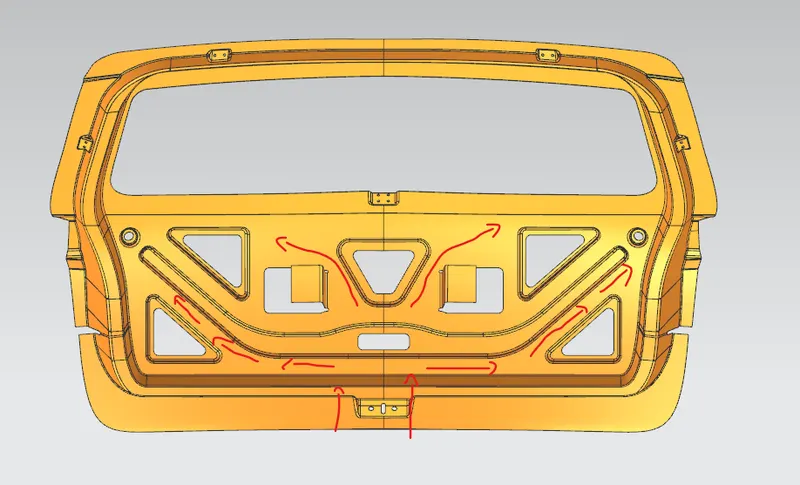
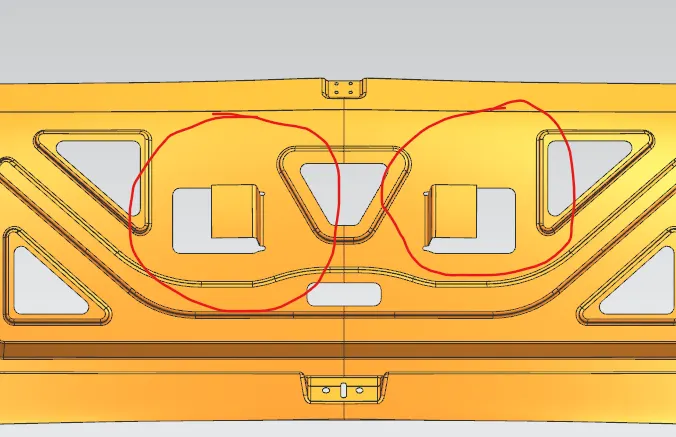
- Later the v or y embosses are created outwards as in case of accidents the force will be dissipated in the direction of the arrows shown in the above picture (outwards).
-
After the concept of the inner panel is developed, then the child components like a hinge, latch, gas-stay locations, and their reinforcements must be designed. Which completes the overall design of the tailgate.
MASTIC SEALANT:
The mastic sealant is used to fix the inner panel with the outer panel which increases the NVH factor and stiffness of the back door.
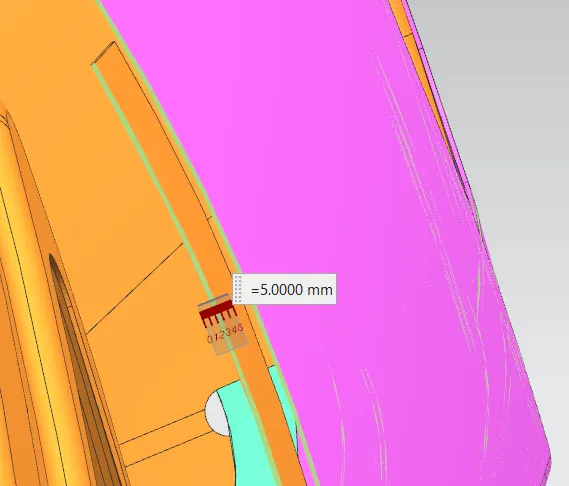
The gap of 5mm is kept for mastics between the inner flange and outer panel.
HINGE, GAS STAY & WIPER MOTOR EMBOSS:
1.Hinge reinforcement
2. Gas stay reinforcement
3.wiper motor reinforcement
4.Latch and striker reinforcement
Hinge,gas and wipermotor reinforcements are made by taking datum plane at an offset distance on the curve and creating a sketch inclined to the inner panel and later trim and extended the surface to create a flat surface .
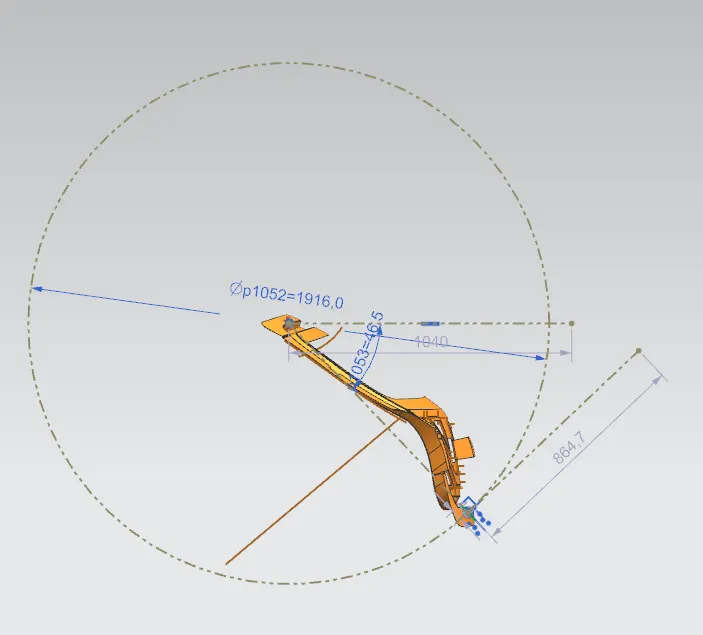
latch and stricker emboss were designed by creating a trajectory that follows the opening and closing of the back door with respect to the hinge axis.
STRIKER POSITION:
The position of the hinge should be perpendicular to the latch when the latch and striker meets. The circle is drawn from the center of the hinge axis to find the path of the striker and positioned perpendicular to the path.
HEMMING:
Hemming and seaming are two similar metalworking processes in which a sheet metal edge is rolled over onto itself. Hemming is the process in which the edge is rolled flush to itself.
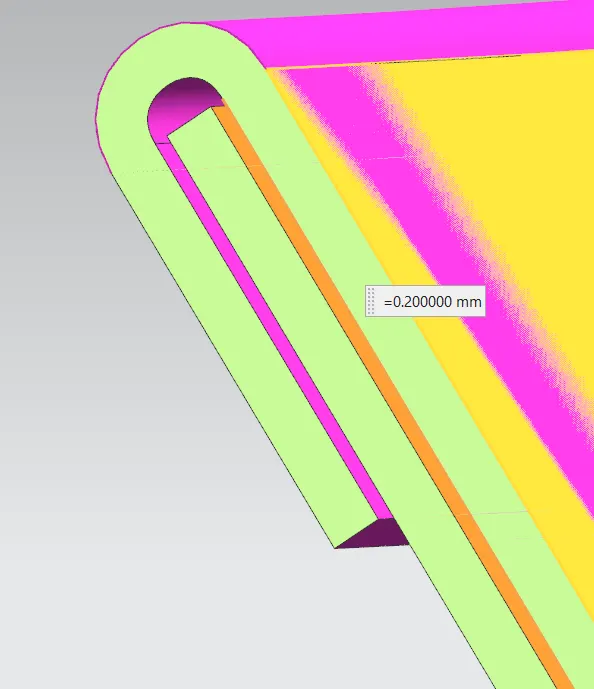
There is 0.2mm gap on both the sides for the sealent to take place.
-
The outer panel was designed as two separate parts named as outer panel upper and outer panel lower.
-
After designing the outer panel the Hemming was created by offsetting the surface with the help of face blend and swept surface.
-
The two separate outer panels will be joined using Blanking.
CORNER RELIEF:
During the hemming process, when giving the Corner Relief helps to control sheet metal material behavior and to prevent unwanted deformation during unbend operations and also helps to reduce the number of passes in hemming.
DESIGNING THE REINFORCEMENTS:
The thickness provided for all reinforcements is 0.75mm.
-
HINGE REINFORCEMENT
-
GAS STAY REINFORCEMENT
-
WIPER MOTOR REINFORCEMENT
-
LATCH REINFORCEMENT
All the reinforcements were created using the same method, first, the linked body was created separately for each with the help of extract geometry and then the required portion was trimmed out and then thickened.
HINGE REINFORCEMENTS
Hinges enable the opening and closing of the back door. One end of the hinge is fixed on the backdoor and the other end on the Roof, on both sides. Hinges can be placed outside or inside the backdoor.The hinge reinforcements are added to compensate for the weak region due to the acting load over it.
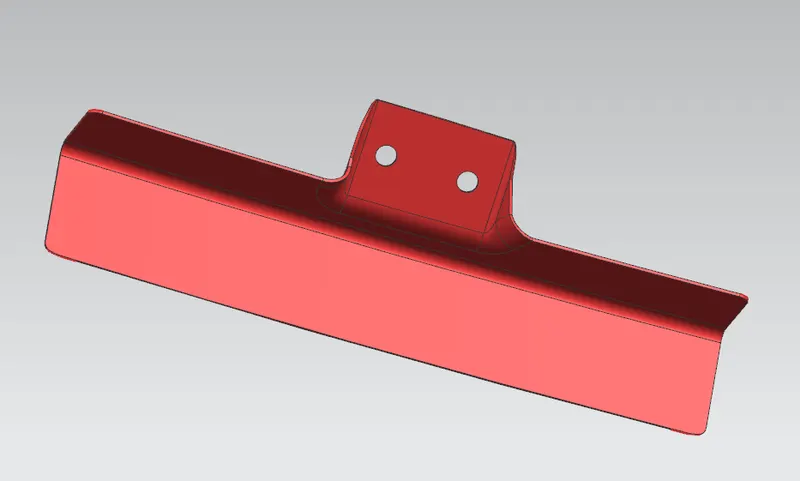
5MM FILLETS ARE PROVIDE OVER THE SHARP CORNERS.
GAS STAY REINFORCEMENTS:
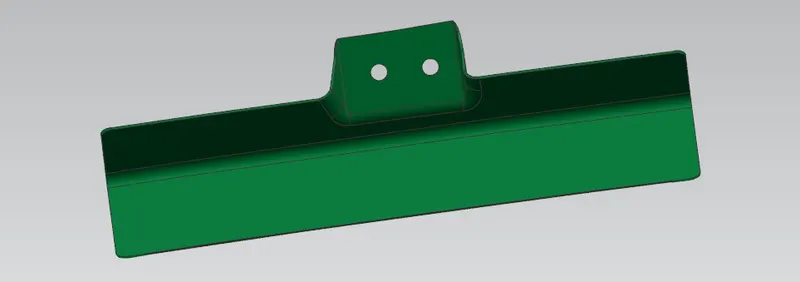
Gas Stay is a device used for supporting the back door in its open position. Gas stay requires no manpower and is engaged into support position automatically as the back door opens. One end of the Gas Stay is fixed on the backdoor and the other end on the Body Side or on the Back door stationary area.Embossing is provided at the Gas Stay mounting area to compensate for weakness and improve strength.
WIPER MOTOR REINFORCEMENT
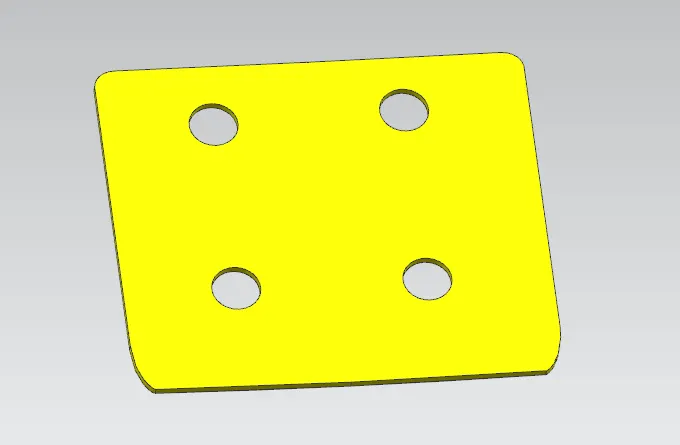
Wiper motor reinforcement is created to mount the wiper motor assembly.
LATCH REINFORCEMENT
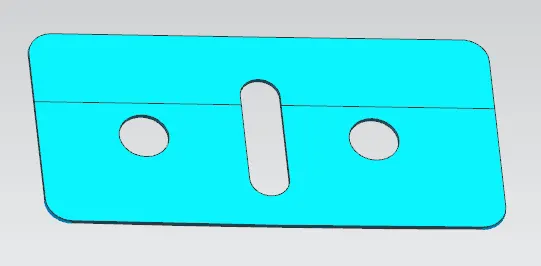
The Latch & Striker forms the locking mechanism of the backdoor with the car. Due to regular opening, closing, and over slamming of the backdoor, there is stress developed in the Latch and Striker area. To compensate for the same, reinforcements are added in this area.
DRAFT ANALYSIS:
Draft analysis shows the wether the produced design is manufacturable or not along the created tooling direction.
It shows results in colours.We get to know wether the design is draftable with the required draft angle or not .If not we need to change the design accordingly.
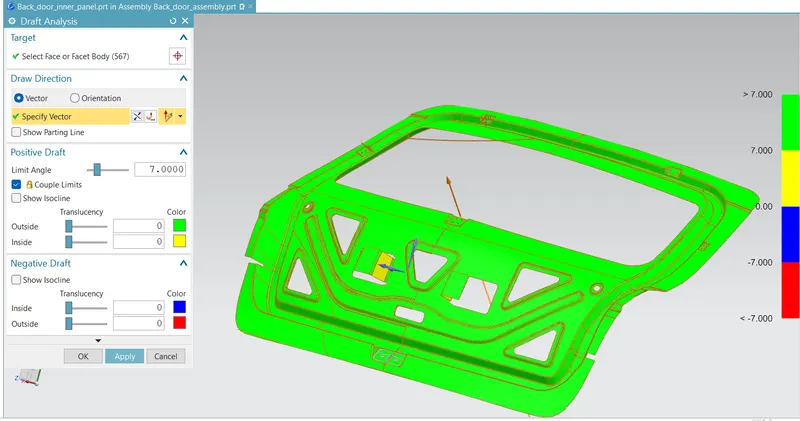
From the analysis its clearly visible that most of the parts can be manufactured with a draft angle of 7 degrees minimum which is shown by green color.
The yellow colored flange is not an issue because its the flange that is made post production by folding the flange for mastics so our design is applicable for further processes.
CAR BACK DOOR ASSEMBLY: