Week 8 - Challenge 6 - Core & Cavity Design
Core & Cavity Design
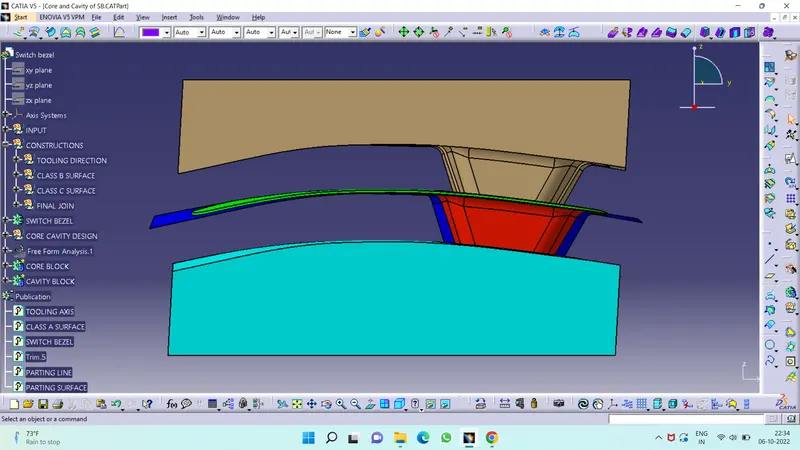
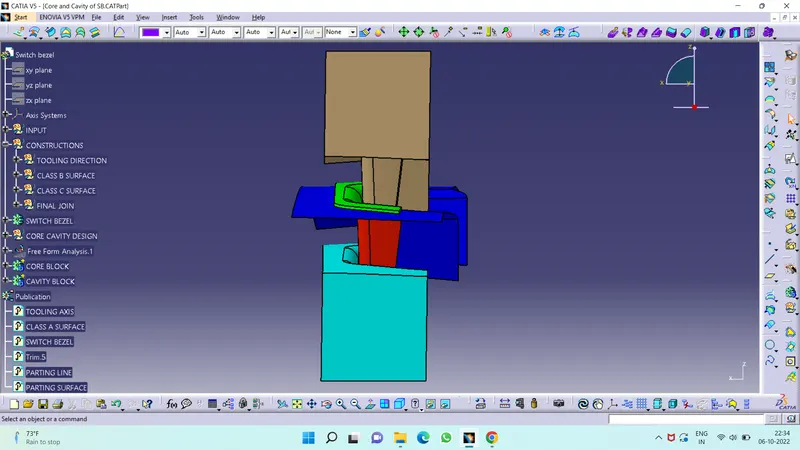
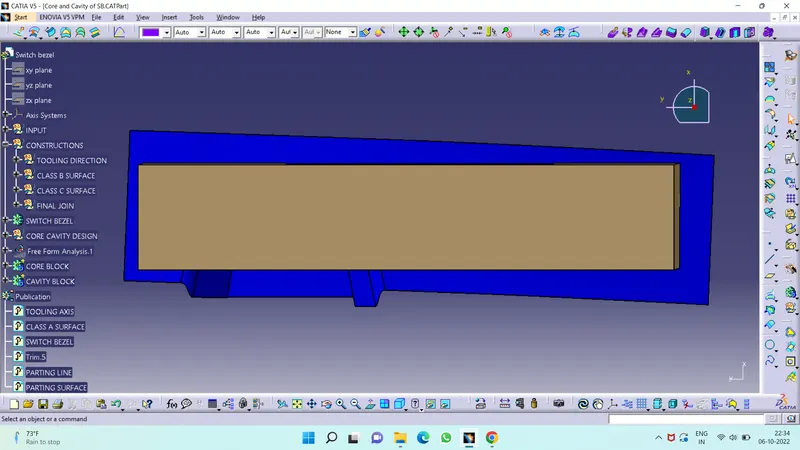
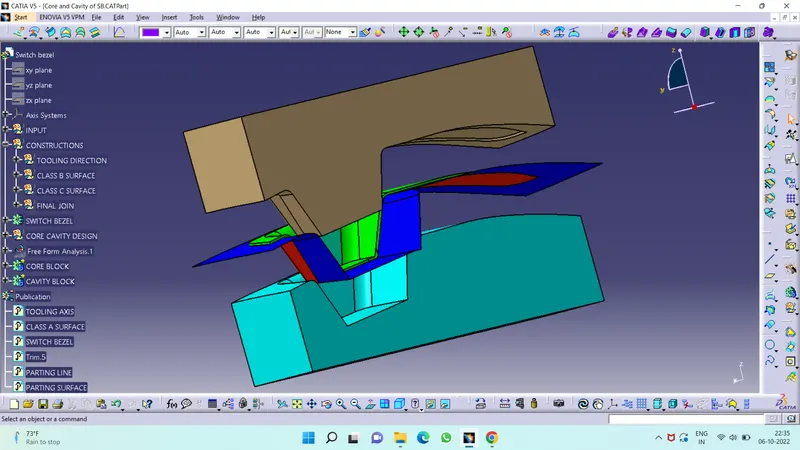
AIM : Create the Core and cavity blocks for the switch bezel component.
Core and Cavity Design for Switch Bezel - Plastic Component Mold
Creating of Core And Cavity Blocks:
- Create a rectangular sketch on the Plane - Normal to the Parting Surface aand Extrude the Sketch to create the Core surface
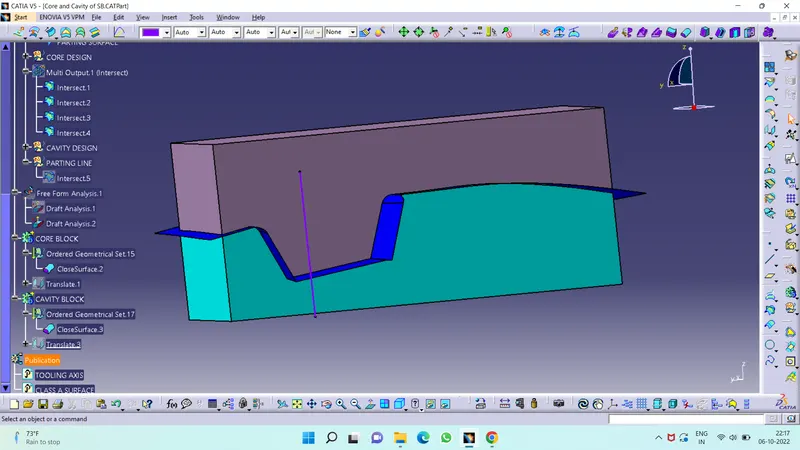
- Extraxct the outer top boundary of the Core Block and Fill the top to create a closed Surface.
- Join the Fill surface and the Extrude of Core
- Trim it with the Parting Surface to obtain the Core Block eclosed Surface.
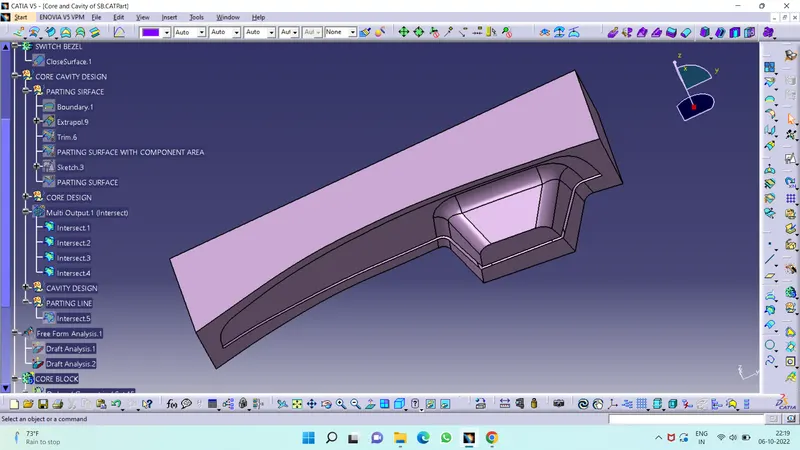
- For creating Cavity Block Extrude the same sketch on the opposite side and create Fill and Join the Surfcace
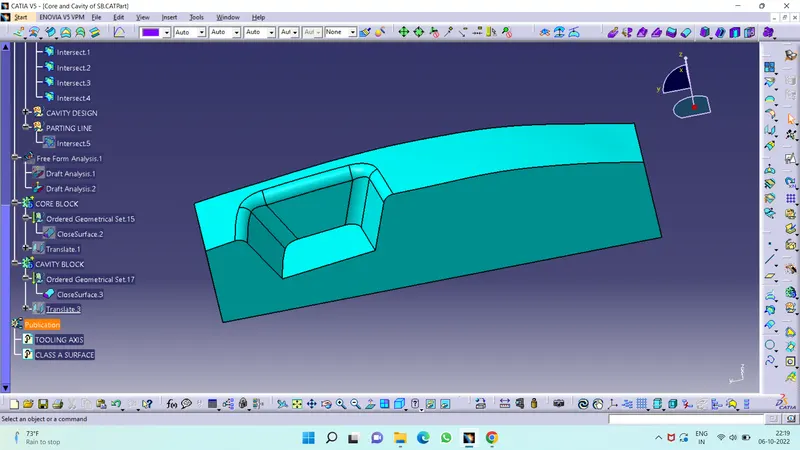
This report demonstrates the design of Core and Cavity Bloacks for an Automotive Plastic Component – Door Switch Bezel using industry principles such as Parting Surface and Parting Line definition, Draft angles, Draft Analysis, Determining and implementing of Tooling Axis, Class A, Class B, Class C surfaces and maintaining the Thickness of the part at 2.5mm. The Molds are designed using Surface Design and Solid Design techniques in CAD package CATIA V5.
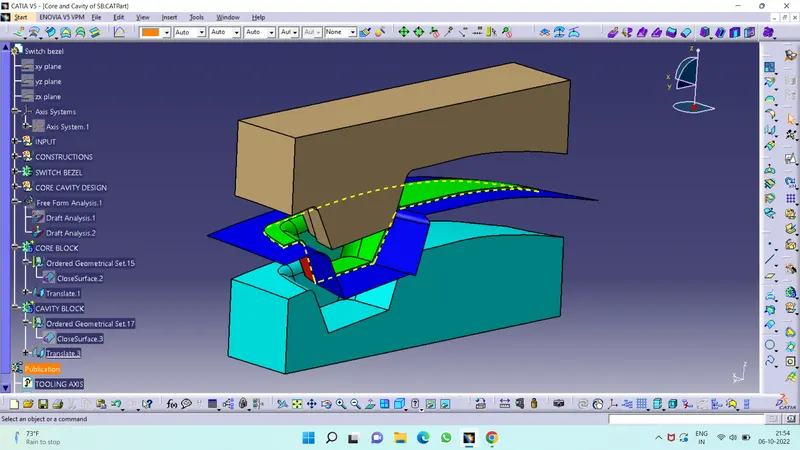
Figure1: Core and Cavity for Switch Bezel
The terms are briefly explained below:
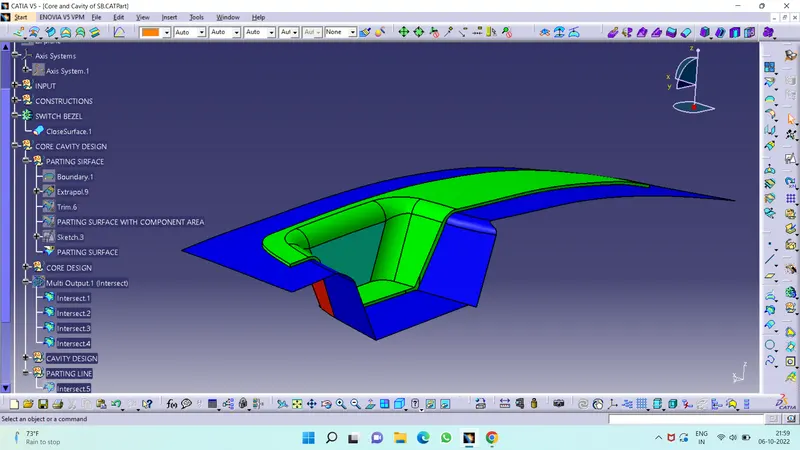
Parting Surface:
- Generally Injection Molding has 2 major components: the Movable Half and the Fixed Half.
- During Injection Molding process, these 2 halves are pressed together tightly to form a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure.
- The pressed surface is called the Parting Surface.
- Usually the parting surface are the biggest projection outline of the part.
- Parting Surface directly affects the Product Quality, Ease of Construction and Operation of the Injection of the Mold, the Mold Design is one of the key factors to the success.
- Design of Parting Surface should follow the following Design Principles:
- Designing the Mold Structures as simple as possible.
- Avoid or reduce side parting as much as possible to reduce complexity of mold making.
- Ease of De-Molding. The plastic component must stay at the fixed half in most cases and ejected by the Ejection System and avoid side De-molding action.
- Ensure Dimensional Acccuracy of the molded parts and try to make parts with similar dimensional accuracy requirements in the same module to reduce manufacturing and assembly errors.
- Ensure Appearance Requirement of the molded parts.
- Flash or mismatch usually occurs on the Parting Surface, so it shoul not be designed on a High quiality requirement Surface.
- Ensure adequate Venting or De-Gassing. If possible Parting Surface should be placed at the end of the Mold Flow. This can be a good advantage for Filling and Venting.
- Parting Surface of Switch Bezel is shown in Figure 1.1.
Parting Line:
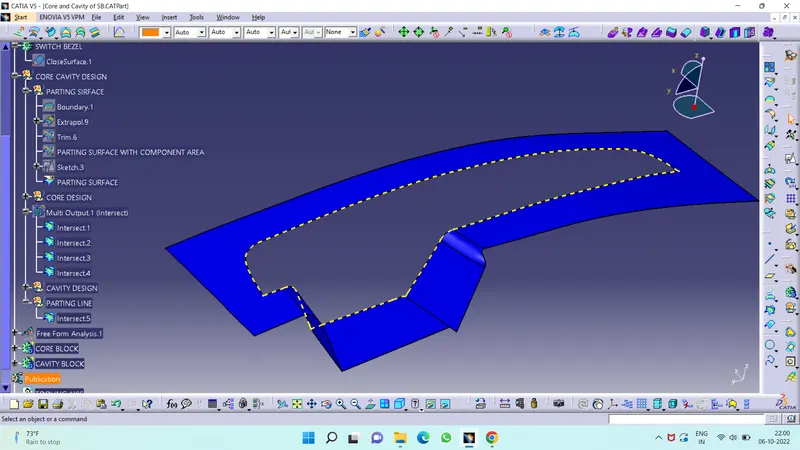
- Intersection of the Plastic Component with the Parting Surface is called the Parting Line.
- It is the Bordered Outline of the Component along the Parting Surface.
- Parting Line of Switch Bezel.
Draft:
- Draft is an angular tapering given at the design stage to every Plastic Component that has to be manufactured.
- It is given in the direction of the Mold Movement.
- The Draft allows the parts to release easily from the mold without creating friction between the surface of component and the core and cavity plates.
- When a Plastic component cools down inside the mold, the natural tendency of it is to shrink and attach to the core or cavity half.
- The movement of mold opening causes friction on the walls of the component as well as the core/cavity blocks.
- This reduces the life of the mold as well as the component itself.
- The component may also have rough surface finish as well as weak structure due to this.
- This problem can be solved by giving draft to the component.
- Most applications require minimum draft angles of around 0.5º to 1º , however 3º draft angles are widely accepted for cost saving purpose.
- 7º Draft angles are given to textured surfaces like Instrument Panels.
- Minimum possible draft angles are given to screw bosses, ribs and stiffeners due to their critical nature.
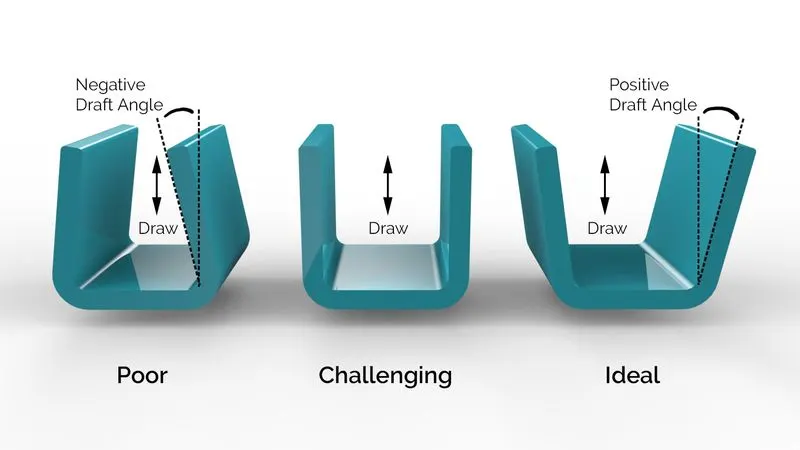
Figure2: Draft Angles
Tooling Axis:
- Tooling Axis is the direction in which the Mold opens and closes. Part Drafts are given along this axis.
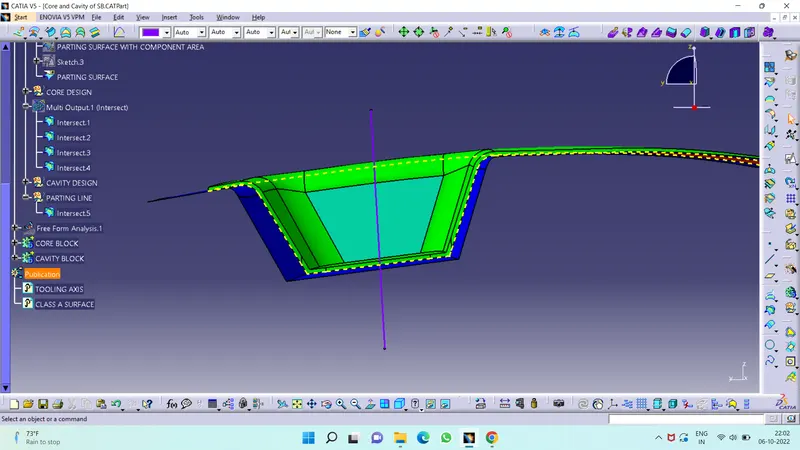
Draft Analysis:
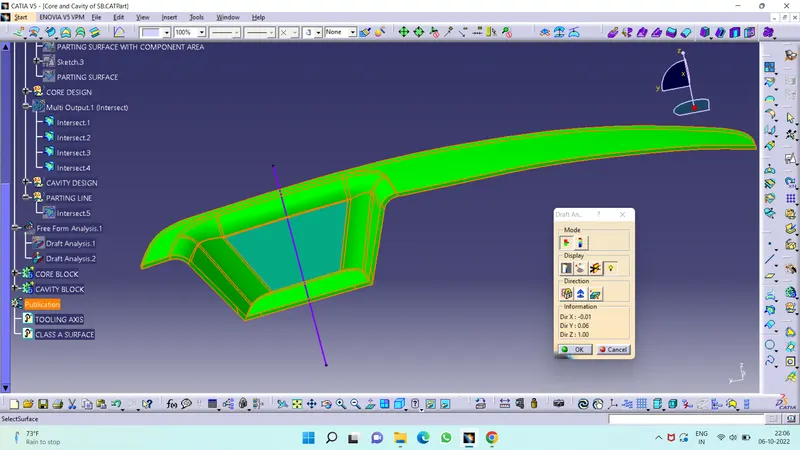
- Draft Analysis is a tool in CATIA which identifies the zones which deviates from the specified values of angles along a defined draft direction using colour codes.
- It highlights the regions of draft using colours.
- Draft analysis is the first step performed after receiving the Class A of the component.
- Draft analysis should be passed in order to make the plastic component manufacturable.
- Acceptable draft angles are used as range for draft analysis.
Class- A Surface:
- In automotive design, a class A surface is any of a set of freeform surfaces of high efficiency and quality.
- It is the visible aesthetic surface of any automotive component.
- Class A surface refers to those surfaces which are visible and abide to the physical meaning, in a product.
- This classification is primarily used in the automotive and increasingly in consumer goods industry.
- It is a requirement where aesthetics has a significant contribution.
- For this reason, the exterior of automobiles is deemed Class-A.
Class- B Surface:
- Class B surfaces are Engineering Surfaces which are invisible to the eyes or often on the back side of the Class A surfaces.
- It is mainly the thickness of the component or Class A.
- These surfaces need to be designed as per the Class A surface i.e., the continuity, thickness of the component, functionality etc should be maintained.
- These surfaces include the main engineering features such as Screw bosses, Ribs, Snaps, Stiffeners and fixations.
- B surfaces also do not contain any aesthetic styling content and textures since it is not visible to eyes.
Class- C Surface:
- Class C surfaces are connectors between Class A and B surfaces.
- This surface connects both A and B surfaces along the Tooling Axis.
- It contains the draft as per the design.
- It is basically the thickened surface between both A and B surface.
- Below Figure 5 shows class A,B and C surfaces: Blue surface is Class A, Purple surface is Class B and Red surfaces are Class C surfaces.
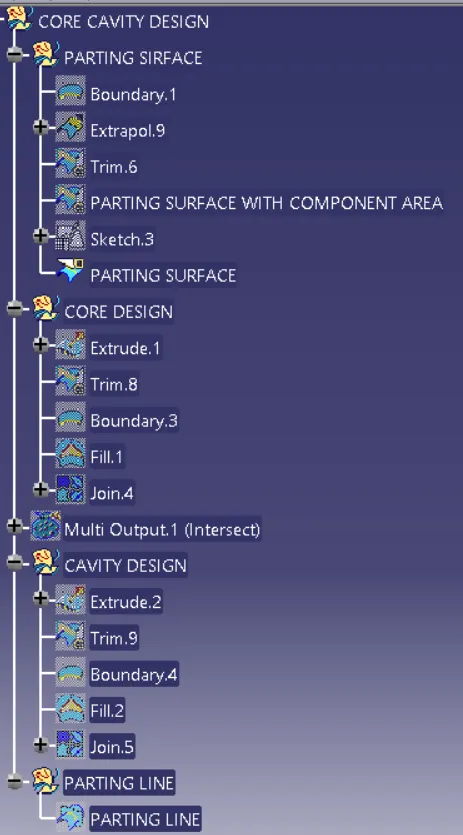
Tree Structure of Core and Cavity Design :
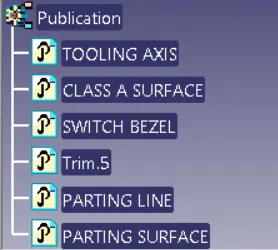
Publications :
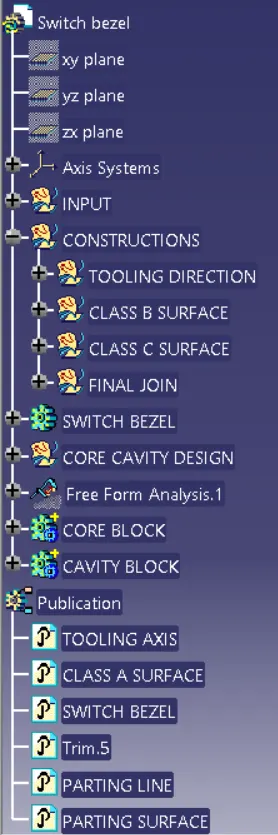
Full Tree Structure :
All Views :
Conclusion:
The Design of Core and Cavity for the Mold of Automotive Plastic Component – Door Switch Bezel is completed using concepts of Parting Surface, Parting Line, Draft angle, Draft Analysis for Class A and Final enclosed surface, Tooling Axis creation and implementation, Class B and Class C creation and conversion to a solid part maintaining the part thickness at 2.5mm.