Week 8 - Challenge 6 - Core & Cavity Design
CORE AND CAVITY DESIGN
Aim: Create the Core and cavity blocks for the switch bezel designed in the earlier challenge.
Design Considerations of Core and Cavity
- Tooling Axis creation
- Checking Draft analysis for created tooling Axis
- Creating parting Surface
- Creating Parting line
- Creating Core Side
- Creating cavity side.
- Tooling Axis:
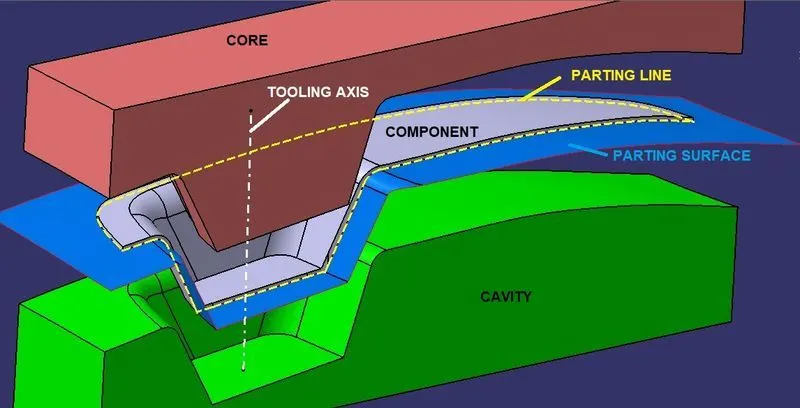
Tooling axis is the axis in which core cavity open during completion of injection molding. To create the tooling axis, we need the proper orientation or view that gives the correct features and draft available in the component.
Component view from the Z direction gives the proper view for the tool to see the features present in the geometry. To create the tooling axis from the Z direction we need the tooling axis from the X direction since it gives the draft available at the slanted part.
The tooling axis created from the X Direction By the following Steps:
- The class A surface is Extracted
- Then the center point is created using the point, on the base surface at 0mm.
- At the point axis system is created.
- After switching the view of the model to the X direction and creating the tooling Axis.
Using the intersect in ZY plane to get the boundary lines.
Then the lines are created along the slant surfaces.
Then these two lines are bisected to get the tooling axis for the X direction.
- Next switching in the Y direction and intersecting the switch Bezel part in ZX direction to get the intersecting Lines.
- Using the axis center point, a line is drawn in sketch mode and it is constrained at the angle of 6 degrees.
- At last, both the lines are bisected to get the final tooling axis.
Below line represent the tooling axis for surface.
- BYSECT METHOD:
FOR DOING THIS YOU SHOUD FIND OUT THE WHAT IS THE BEST TOOLING DIRECTION. FOE DOING THAT TO ROTATE THE PART AND SEE ALL DIRECTIONS AND CHOOSE THE WHICH DIRECTION WILL BE COMFORTABLE.
THEN CREATE THE POINT ON THE BASE MOSTLY CREATE THE POINT WHERE THE HOLE OR POCKETS ARE GIVEN. AND AFTER THAT INSERT TOOLING AXIS IN THAT POINT.THEN FIRST SEE IN X DIRECTION IT ILL CLEAR THE ALL FACES OF PARTS IF NOT CREATE A PLANE AND INTERSECT TO EACH OTHER. THE FALLOWING WINDOW WILL BE APPEARED.
THE CREATE THE MEAN LINE. AND GO TO Y DIRECTION AND DO THE SAME PROCESS WE ARE DONE IN X DIRECTION.
THEN BYSECT THESE ALL LINES TO GET THE MAIN TOOLING AXIS. THIS TOOLING AXIS CAN BE CLEARED ALL FACES OF THE PART.
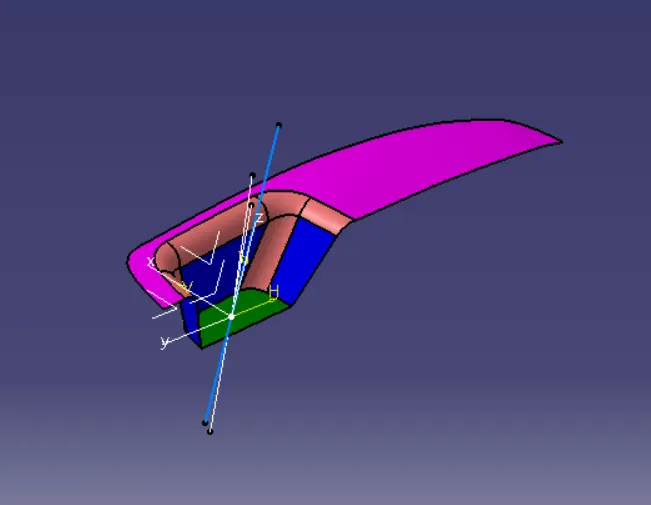
- Draft Analysis:
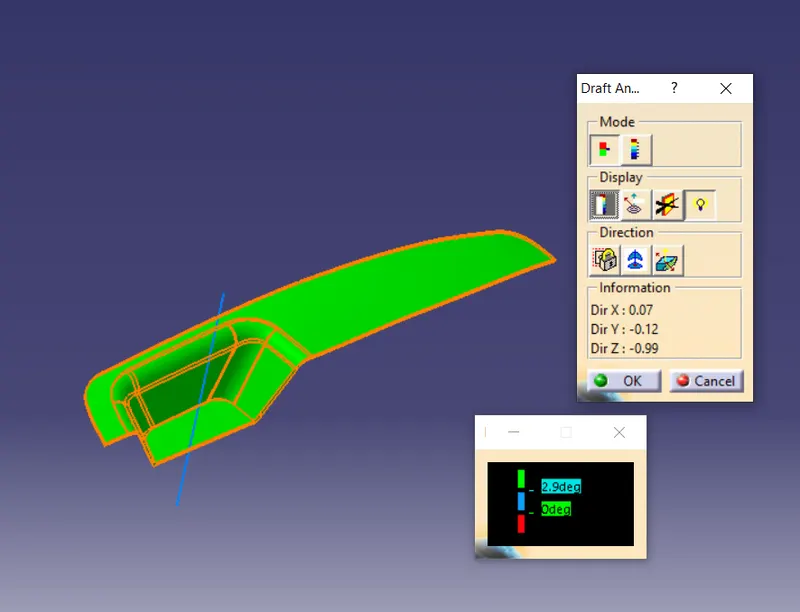
Draft analysis enables you to detect the part we drafted will be easily removed. This type of analysis performed on the base of color ranges identifying the zones on the analyzed element where the deviation from the draft direction at any points, corresponds to specified values.
- Go to insert
- Click on the compass icon and align it with the tooling axis and click on the surface, we will get our result
- Parting Surface:
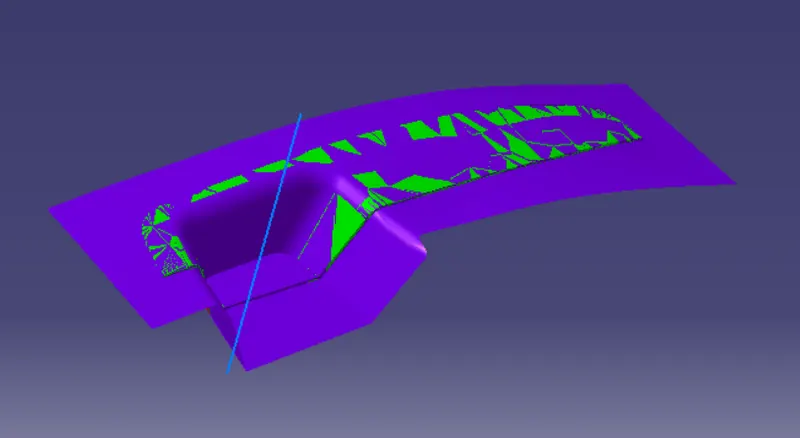
Generally, injection mold has two major components: the movable halves and fixed halve. During injection molding process these halves are pressed tightly from a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface called as parting surface, usually parting surface is the biggest projection outline surface of the part.
Parting surface design directly affects the product quality, ease of construction and operation of the injection mold
injection mold has two major components one is core and another is cavity .during the injecction molding process, these two halves are pressed tightly from a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface are called parting surface , usually parting surface are the biggest projection outline of the part.
- BOUNDARY
- EXTRAPOL
- TRIM
- PARTING SURFACE WITH COMPONENT AREA
- PARTING SURFACE
- Parting Line:
Parting line are where the two halves of the mold meet. This generally create a physical line on a part that is both visible and noticeable to the touch. These lines however can be hidden or minimized when placed along edges of the part. It is represented by dotted line in the below picture
injection mold has two major components one is core and another is cavity .during the injecction molding process, these two halves are pressed tightly from a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface are called parting surface , usually parting surface are the biggest projection outline of the part.
parting line:
it is the area in which parting surface and component meets Or it is a junction between core and cavity
and the parting surface has some set of rules because the product quality mostly depends on the parting surface.
DESIGN PARTING SURFACE SHOULD FOLLOW THE FOLLOWING PRINCIPLES :
- Design the injection mold simple as possible .Avoid or reduce side parting as much as possible to reduce complexity of the mold making.
- Ease of de-molding as far as possible, for instance the plastic parts should stay in fixed halve of injection mold and should ejected by ejection system avoid , side de-molding action,
- Ensure the dimension accuracy of the molded parts ,Try to make the parts similar dimension accuarcy reqirements in same mold to reduce manufacturing and assembly errors .
- Ensure apperance reqirement of molded parts,finish or mismatch usually occurs on parting surface , so the parting surface should not be designed on high quality requiremnent surfaces.
- Ensure adequate venting.If possible parting surface should be place at the end of the mold flow.This is going to be advantage of fillng and venting.
- INTERSECT
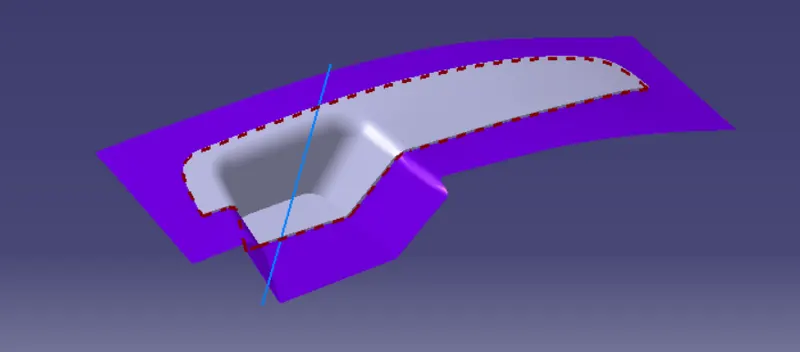
PARTING LINE AND SURFACE.
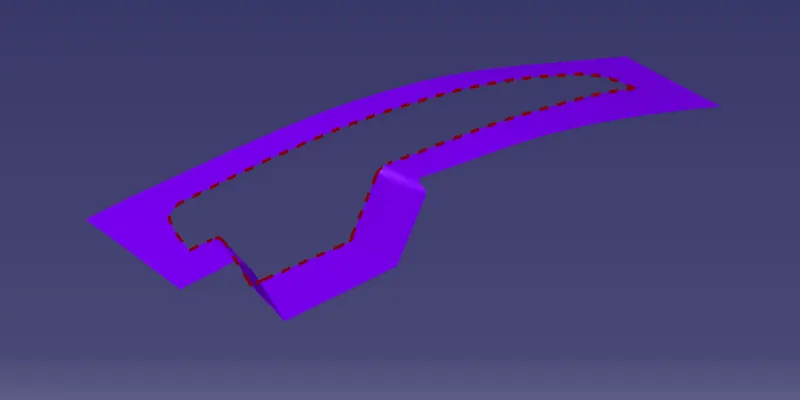
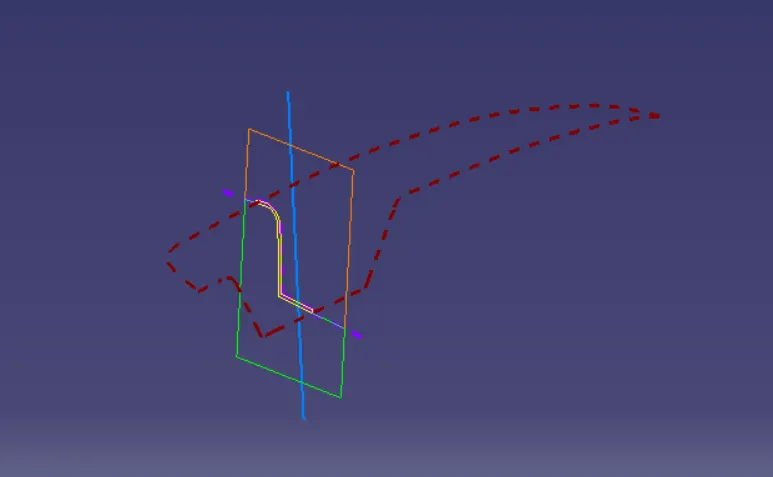
PARTING LINE.
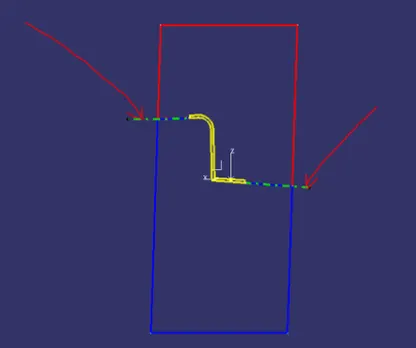
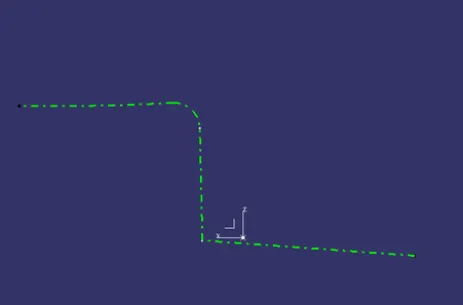
Mold and Cavity profile.
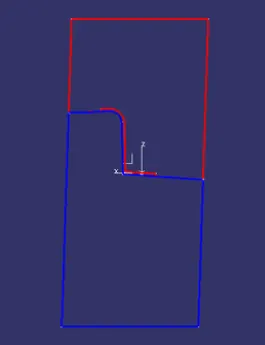
- CORE & CAVITY DESIGN.
The Mould Core & Cavity are the shaped sections in either half of the mould tool which give the plastic product its final shape.
The hot molten material is injected into the core & cavity and then sets hard into shape. The design of the core & cavity is essential in the correct formation of the product. The sequence of events during the injection mould of a plastic part is called the injection molding cycle.
The cycle begins when the mould closes, followed by the injection of the polymer into the mould cavity.
A core is usually made of the best quality sand and is placed into the desired position in the mould cavity. Core prints are added to both sides of the pattern to create impressions that allow the core to be supported and held at both ends.
- PART DESIGN OF CORE:
- SKETCH
- EXTRUDE
- TRIM
- FILL
- JOIN
- MULTI OUT PUT(INTERSECT)
- The core design is started with extracting the parting surface that becomes the datum for the core and cavity. The parting surface in most of the cases is kept at the B class surface to avoid close and tight contact between the core and cavity.
- At first, the A-class surface is extrapolated with some length and later it is trimmed with a C surface
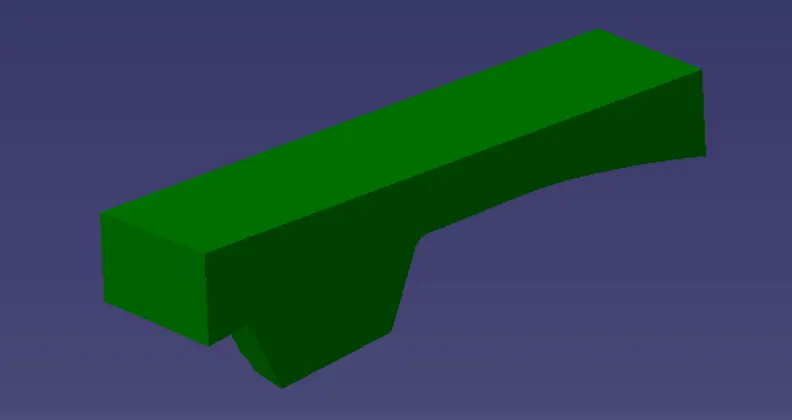
PART DESIGN OF CAVITY.
- EXTRUDE
- TRIM
- BOUNDARY
- FILL
- JOIN
- The cavity is the part where the injector and filling of the molten plastic happens. The cavity block is prepared by first extruding the outer boundary along the tooling direction.
- A mold is a hollow form typically made from stainless steel that has plastic injected into it to manufacture a plastic part.
- The plastic is inserted into the mold cavity, which is a hole in the mold shaped like the desired part.
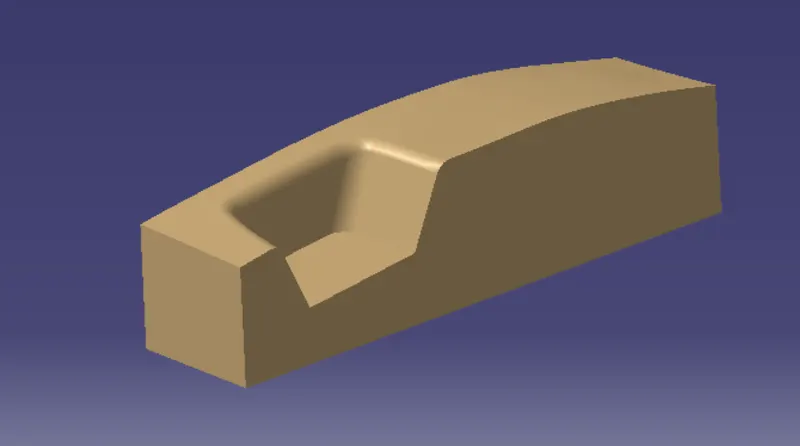
CLOSE BODY SURFACE OF CORE & CAVITY.
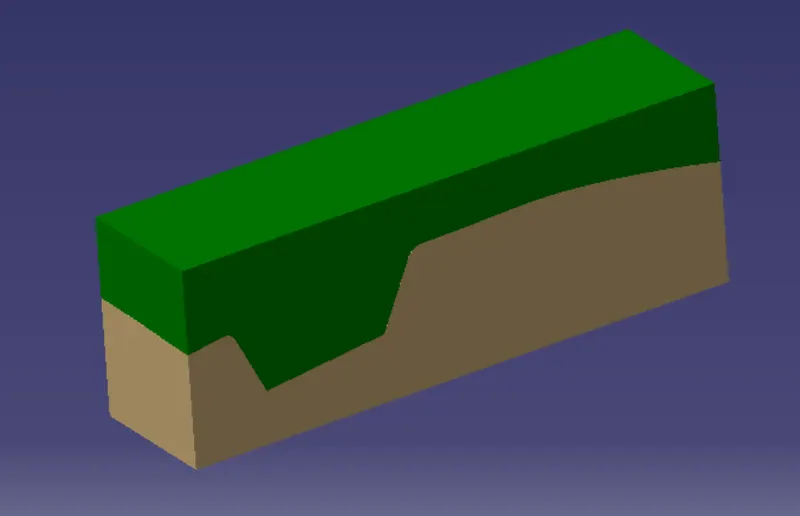
Mold, Cavity and the solid part:
Isometric view
Front view.
Left side view. Top view
Final view.