Week 8:- 3D Finishing Challenge 2
Aim:
- Perform 3D finish for all units of car panel fixture ssembly design.
- Create Rough locators for fixture assembly.
Introduction:
3D finish is process where the design is being completely finish and to be ready for final simulation and 2D detailing.
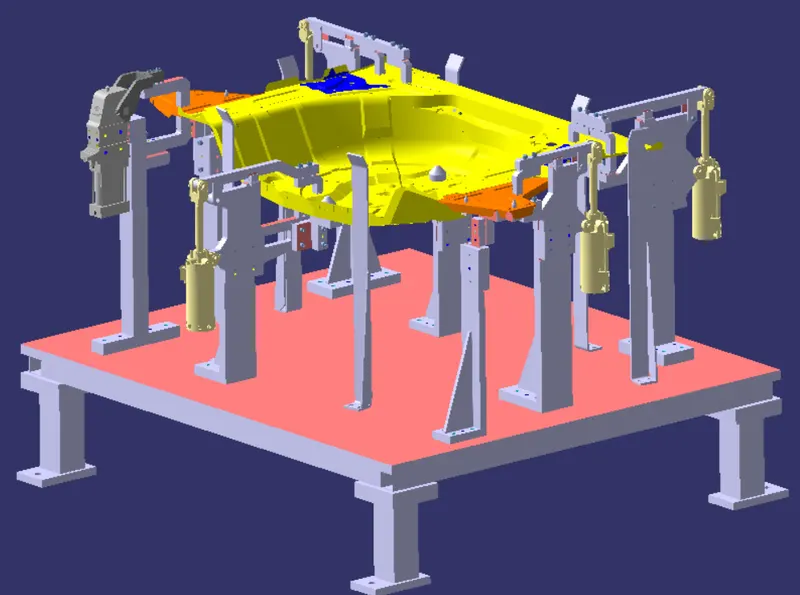
Points to be considered while finishing the Design:
- Hole concentricity and hole sizes: All parts Hole concentricity should be checked & confirmed for easy assembly while finishing the parts.
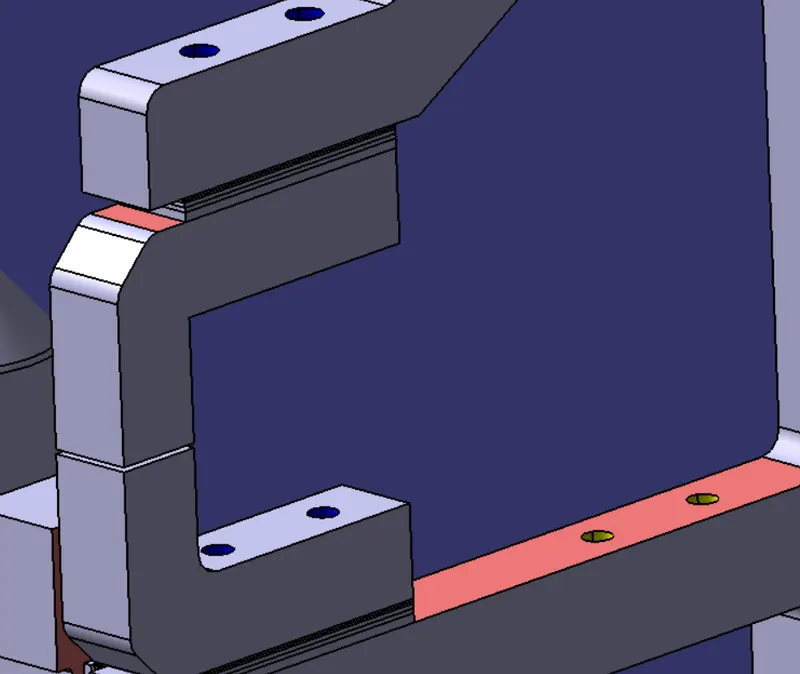
- Machining area.
- Nominality : All units dimensions shoild be maintained nominal to facilitate easy assembly of the unit.
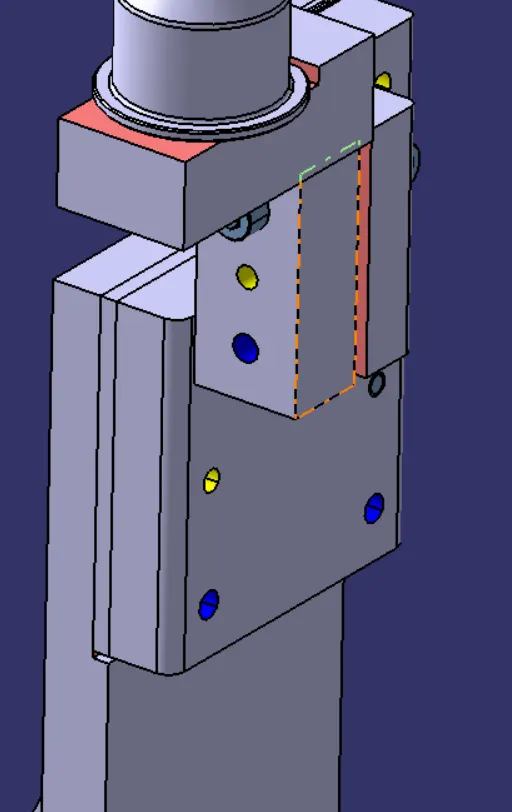
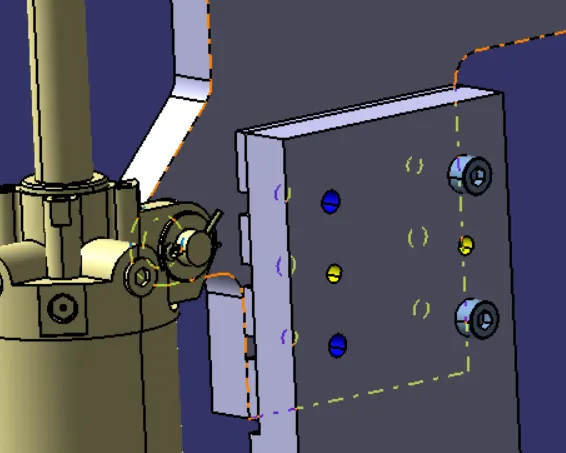
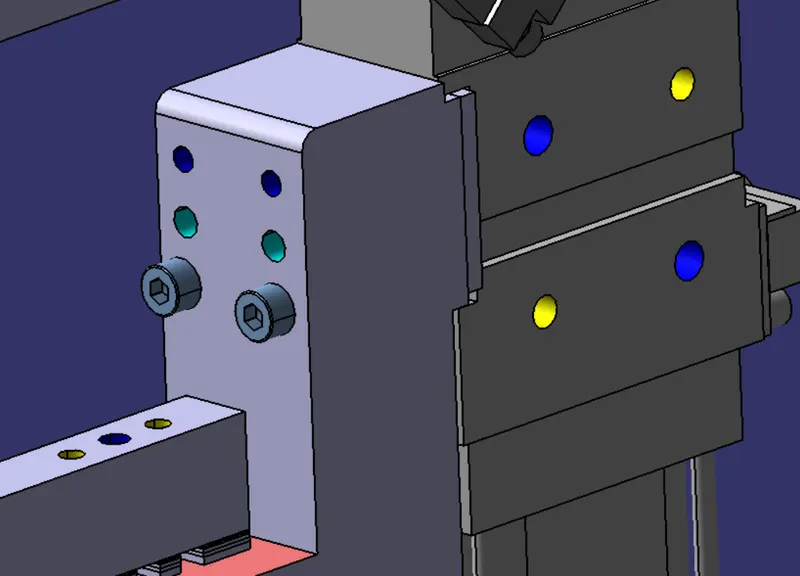
- Holes coloring standard : The holes should be coloured according to the standards with different colour for different hole sizes.
- Pneumatic lay-outing : Proper layouting of the pneumatic or cables.
- Gap cheching : To check if there any clash or gaps between the 2 assembled parts.
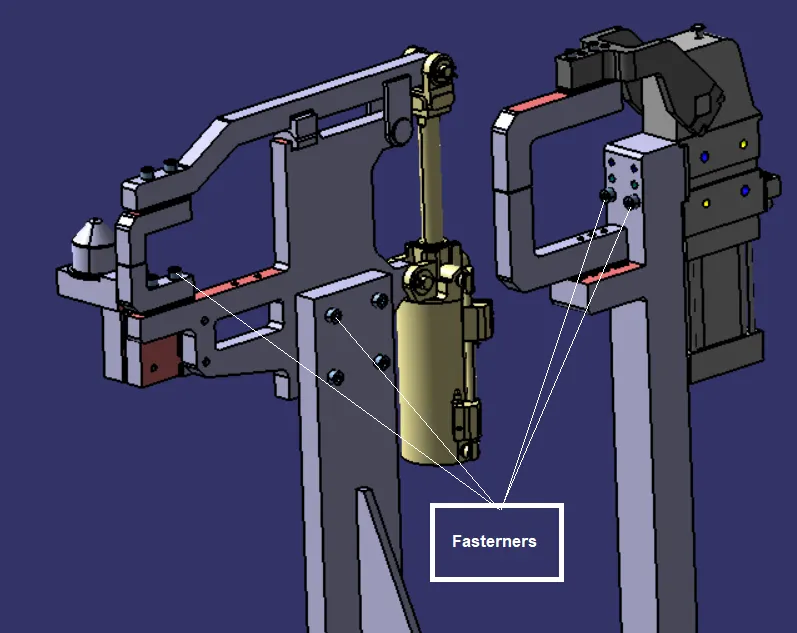
- Fastener implementation: Fasteners should be implimented in all unit as per the requirement & load on the part. like bolts, washers, screws etc.
- Avoid clash between different parts: Proper gap should be maintained between parts to avoid the clash.
- Mylars splitting as per panel pofile: Mylar splitting should be confirmed while finishing the design (It shuld be split with reference to the panel).
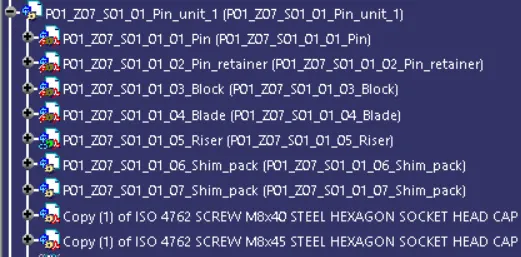
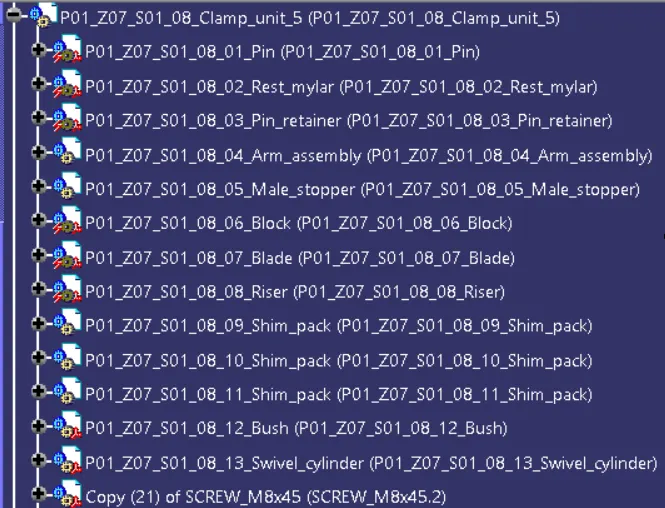
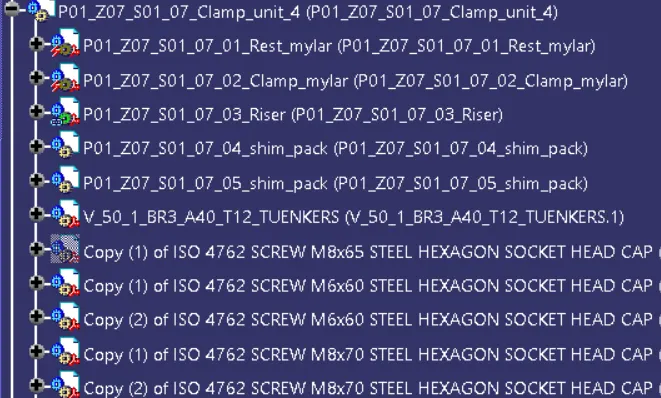
- Proper renaming of parts and assemblies as per the standard.
Rough Locators:
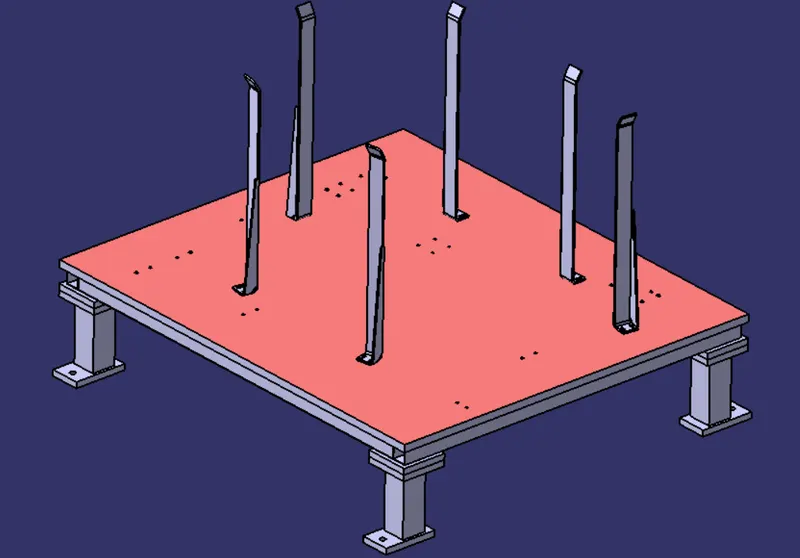
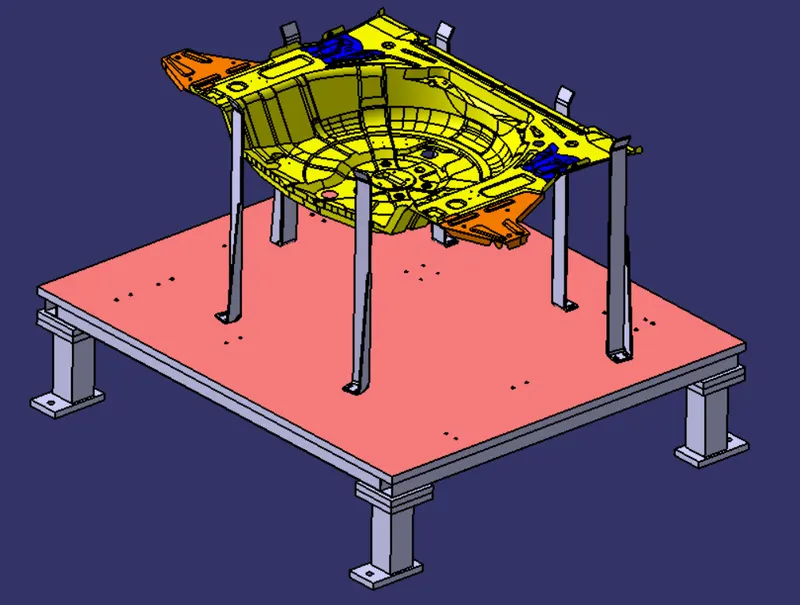
Rough locators are elements that aid the operator to guide / locating the car panels while loading onto the fixture and ensure a fool-proof assembly. Locating refers to the desired location where you want the workpiece to be when it is getting worked on either by a person, team, or robot.
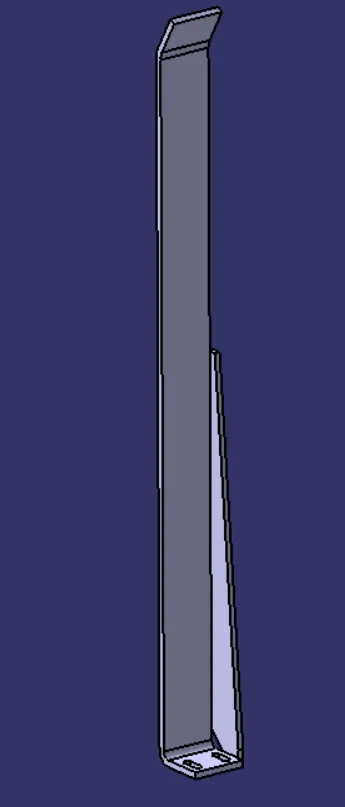
Material used uded for rough locators are MS or similar metal.
Following points need to be considered while designing the rough locators:
- Height of the rough locator should not be more than ergo height of the fixture.
- The entry or top point of the locator should be 10mm - 15mm above the paenl surface.
- Rough locator should have a adjustment in the direction of guiding plane.
- A gap of 2mm should be maintained between the locator and the panel at the time of designing.
- Rough locators can be rod type or flat type depending upon the standards and other conditions.
Positioning of rough Locators on the Base Plate:
Gun Study:
- Welding is predominately used in automobile industries and requirements for fixture that ease the welding process is a continous development. car body in white is a complicated steel structure including 300-500 sheet metal with complex shape are assembled bt means of welding in a high rhytm.the foremost structure taken before starting before starting the design of welding fixture is to arise at spot.
- The location and orientation of the critical units of the fixture including clamp and locator are decided on weld spot distribution.the weld spot for front door inner side panel bracket assembly are located as shown with respect to panel.
- The device used to make spot welding on the panel is called weld gun.
- The gun may differ depending upon the application fixtue wiil be designed by considering weld spot distribution of the panel.
Points need to consider during the gun study:
These are a few points which we need to take care of when we perform the gun study
- The axis of weld spot along welding direction must be normal to the weld
- The gun study should be performed once before the actual simulation
- The position of the gun should be manipulated first in case of a collision with other parts.
- If the position of the gun cannot be manipulated further, the location of the part must be modified or it can also be modified depending on the situation The entire given weld points must be cleared.
- During the gun study, we have to consider client cycle time and we have to maintain the cycle time compared to client requirements.
Fixture Design:
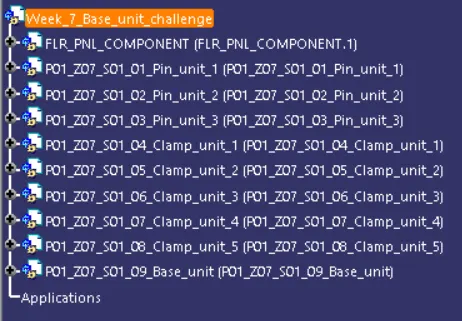
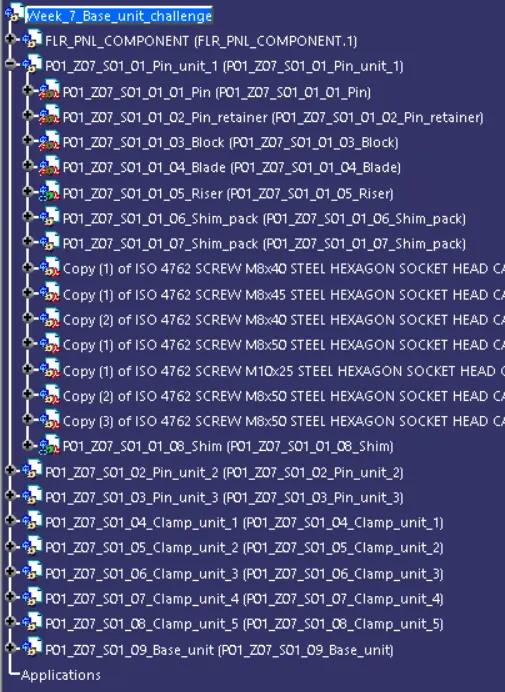
The first step in the finishing process of the design is renaming / structuring the family tree comopenents in series as shown in below images,
Base unit:
Base unit is the fundamental component of the fixture because all other components are mounted over its so every fixture have base unit . The base unit design is different accordign to the panel.Design of clamp system ,location system etc.
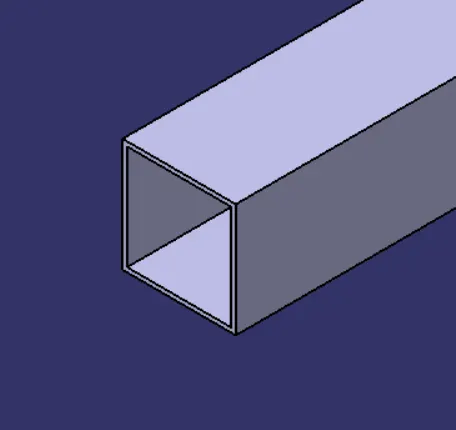
- Trunking channel:
Trunking channel is a basically duct which accomodates all the pneumatic and electrical hoses and wires for the unit. It protects the wires / cables from damage.
- Base plate:
Base plate is a machined plate of 25 to 40mm thickness made of steel and aluminium, on to which the holes are drilled to mount the individual units like clamp unit, pin unit etc.,
- Pedestal:
It is a component which connects the base plate to the floor plate. Pedestal is a standard part in general and it can be welded to the base plate.
- Floor plates:
Floor plate is grouted to the floor with fixed bolt on the ground. Floor plates are also called as foundation plates.
- Eye bolt:
An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it inrder to lift the unit. The eye bolt should be placed such that it does not harm clamp / pin units.
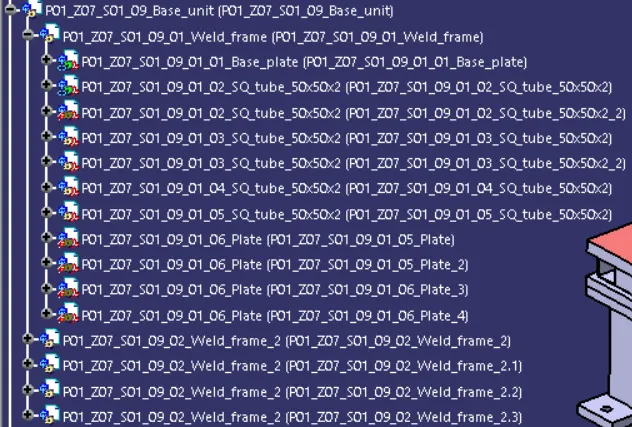
Renaming of parts list in base unit:
Checking the nominality of the Holes on the Base plate:
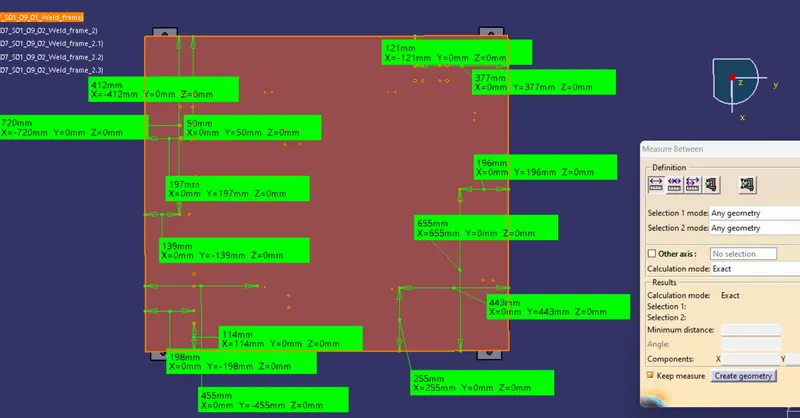
In the above image the base plate surface colour is changed desribing the machining surface.
The holes are assigned with a colour according to the uses as shown below:
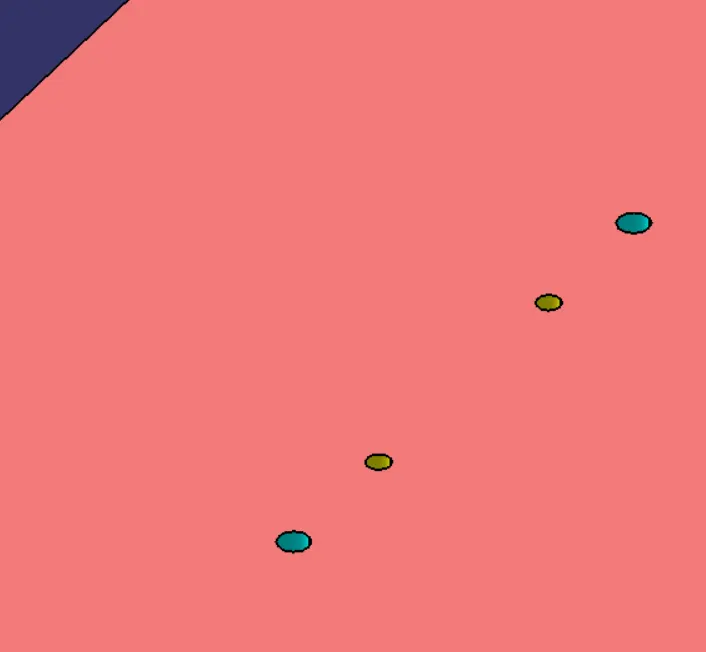
Dowel Hole: Blue Colour
Threaded Hole : Yellow colour
|
Checking Parameter |
Action |
|
Rename of the design tree |
Done |
|
Mark Machining Area |
Done |
|
Nominality |
Done |
|
Holes colouring standard |
Done |
Pin Unit:
Fixed pin unit is a unit designed to locate the car panel using pins. Pin, pin retainer, shims, blocks, blade, riser are the part of fixed pin units in general . pin retainer is used to hold the pin firmly.
The parts of fixed pin are:
- Pin
- Pin retainer
- Shim / spacer
- Block
- Blade or Adapter plate
- Riser.
Pins
- Pins are used for accurately locating the part to welded in an assembly.
- The holes in the part of the assembly are inserted on these pins.
- The pins constrain the degrees of freedom of the part of the fixture.
- The diameter of the pins has tighter tolerances as compared to the diameter of the hole in the part.
- The Pin can be either round or diamond-shaped. Generally, diamond-shaped pins are used to avoid over constraint.
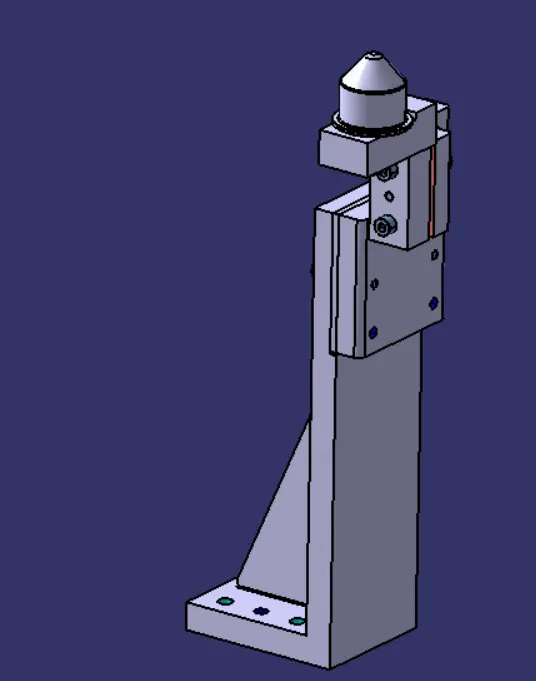
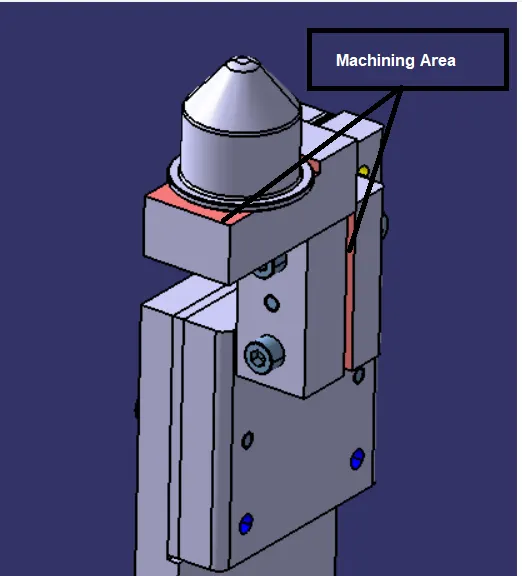
Marking of Machining area:
Hole colouring standard:
 .
Proper Renaming of Parts:
|
Checking Parameter |
Action |
|
Rename of the design tree |
Done |
|
Mark Machining Area |
Marked |
|
Nominality |
Done |
|
Holes colouring standard |
Done |
|
Fasteners Implementation |
Done |
Clamp units:
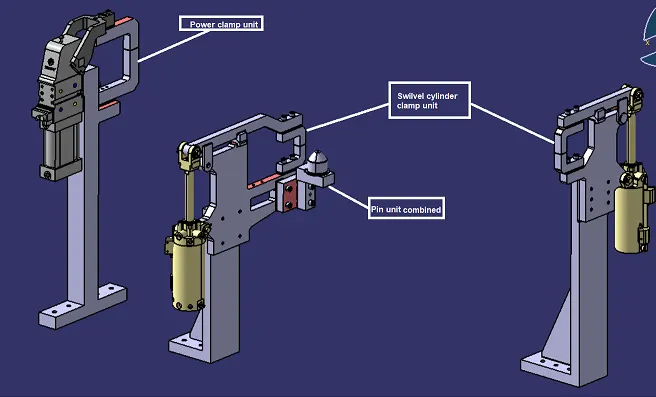
A clamp unit is a unit designed to clamp/hold the car panel with NC blocks/Mylars/rest by using a pneumatic cylinder. Clamp arm, finger, Rest/backup, L-block, shims, riser, pneumatic cylinders are the typical parts of clamp unit.
Here 3 different types of Clamp units are used such as Power clamp unit, swivel clamp unit and combination of clamp and pin unit as shown in below befure:
Proper Renaming of Parts:
Hole colouring standard:
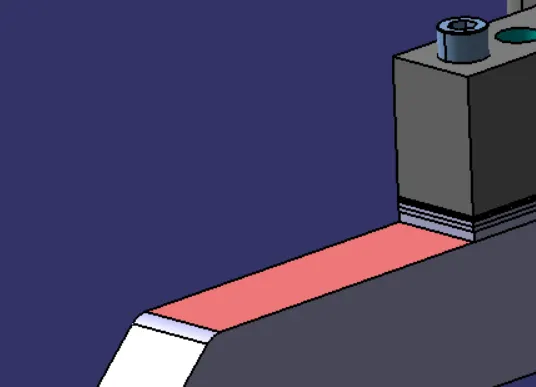
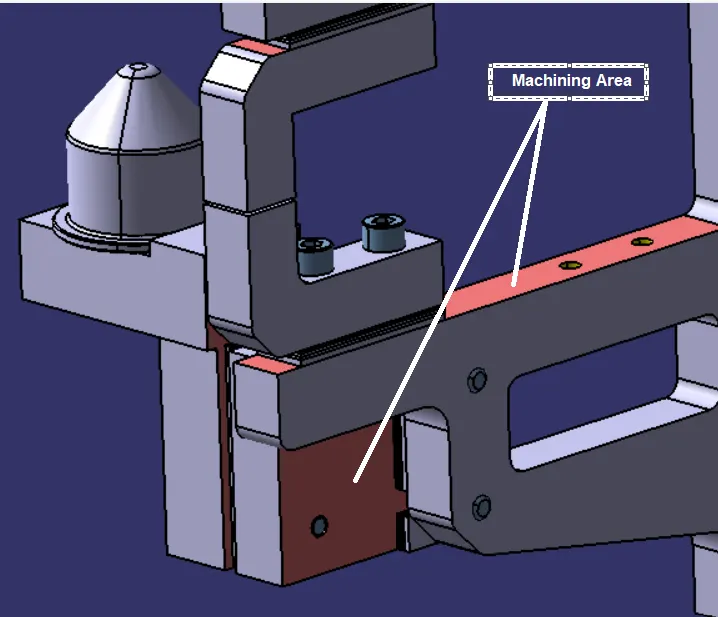
Marking of Machining area:
Fasterner Implementation:
|
Checking Parameter |
Action |
|
Rename of the design tree |
Done |
|
Mark Machining Area |
Marked |
|
Nominality |
Done |
|
Holes colouring standard |
Done |
|
Fasteners Implementation |
Done |
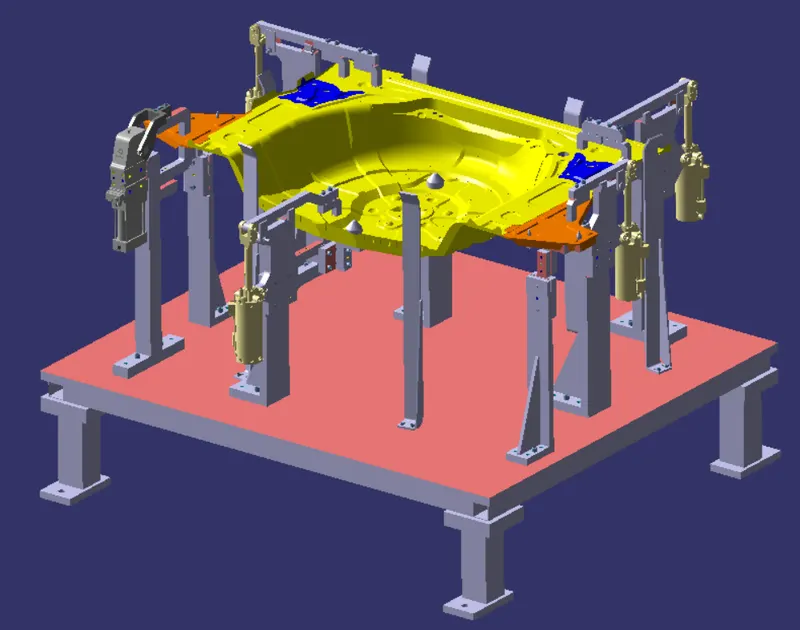
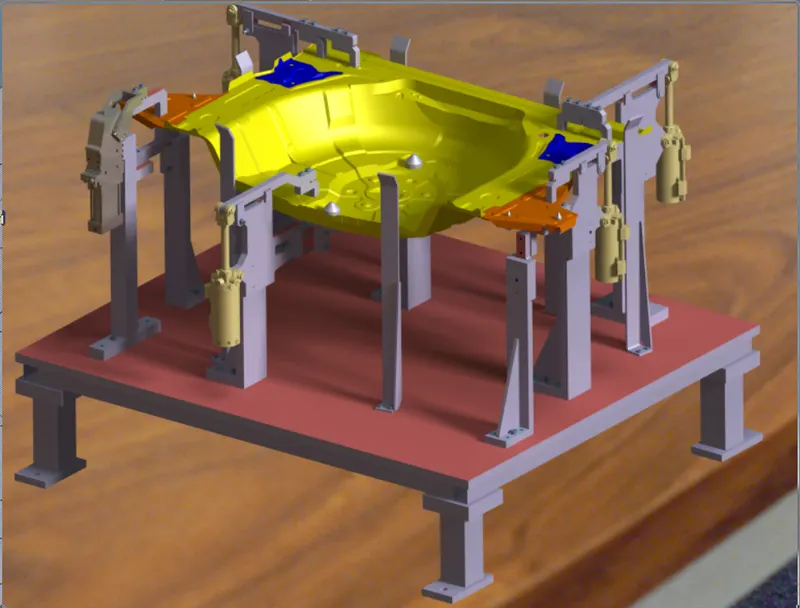
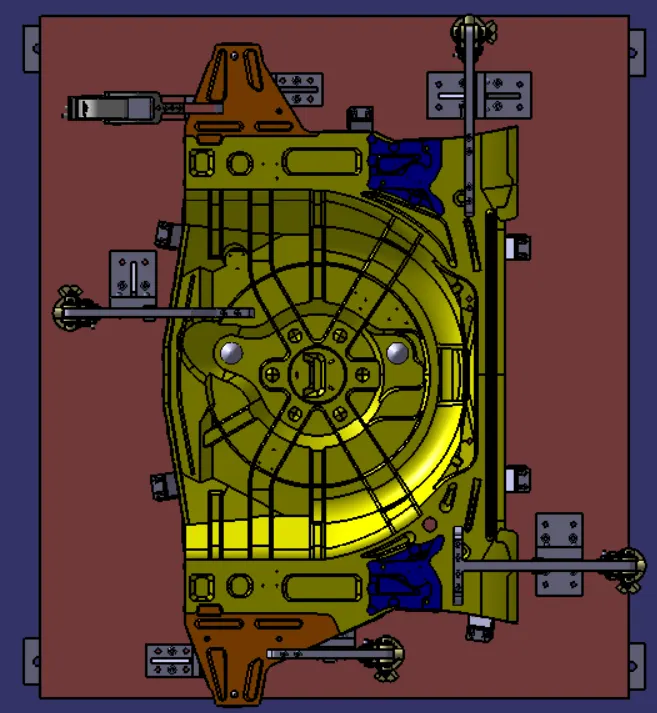
ALL THE UNITS USED IN THE ASSEMBLY AFTER 3D FINISHING:
Conclusion
- 3D finishing is performed on the designed Assembly of Fixtures.
- Rough Locators were designed for the given panel.