Week 6:- Clamp Unit & Pin-Clamp Unit Design Challenge
PROJECT : CLAMP UNIT & PIN-CLAMP UNIT DESIGN
Aim:
The aim of this project is to design 3 Swivel clamp units and a Pin-clamp unit for the given car panel along with different risers, blades and mylars.
Abstract:
In this project, 3 different swivel clamp units are designed with different risers, blades,mylars along with a pin-clamp by using power clamp. For the swivel clamp units swivel type cylinders are used. The stroke of the cylinder is maintained as 100 mm. The design is done considering the fundamentals of pin unit design and 3-2-1 principle along with the clamping forces of the cylinder.
Software used: CATIA V5
Introduction:
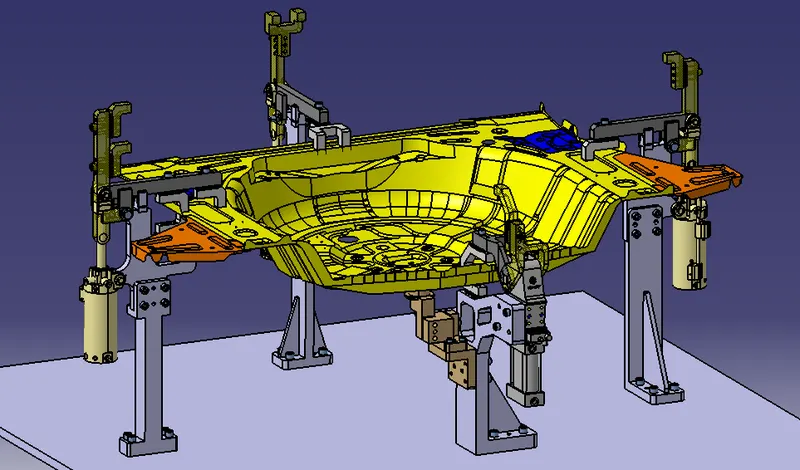
Fig shows: Various units of the design
CLAMP UNIT:
- A clamp unit is a unit designed to clamp/hold the car panel with NC blocks/Mylars/Rest by using a pneumatic clamping cylinder.
- Some of the parts of the clamp unit is clamp arm, finger, rest/backup, L-block, shims, Risers and Pneumatic cylinders.
- Types of clamp units:
- Power clamp unit
- Swivel cylinder clamp unit
Swivel clamp unit:
- Swivel clamp unit is designed to clamp/hold the car panel with clamp/rest mylar by using a pneumatic clamp cylinder.
- Clamp mylar is connected to pivoted clamp arm which is connected to the pneumatic cylinders. Down stroke of the cylinder opens the clamp.
- Usually clamp open posotion is 90 degree.
- Swivel clamp consists of clamp/rest mylars, blade, clamp arm, stopper, pivot plate, riser and shims.
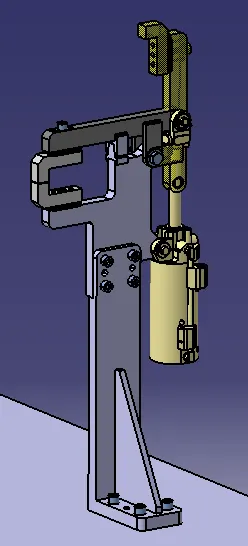
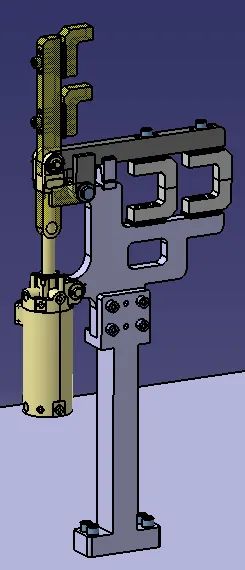
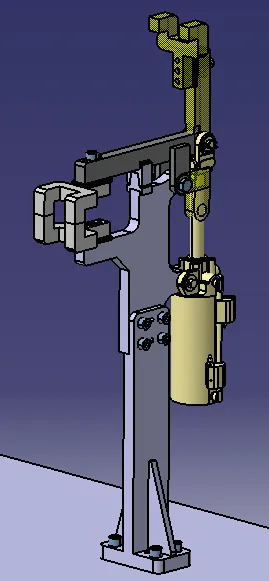
Fig shows: Swivel clamp units
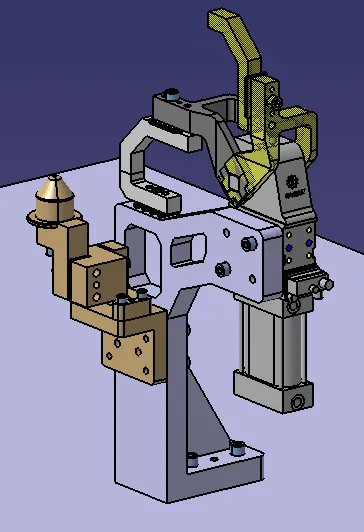
Fig shows: Clamp-pin unit
Fundamentals of designing a clamp unit
- It is preferred to design clamp unit with pivot centerline in-line with clamp surface. When possible upto 25mm offset can be acceptable.
- For sigle angular clamping, it is recommended that the centerline of clamp pivot be positioned on plane that is created by surface being clamped, upto 15 degree off normal pivot location can be used in extreme cases where recommended clamping condition cannot be satisfied.
- There should be adequate space between the cylinder & the riser to allow the swinging motion of the cylinder while opening & closing.
- Clamp-pin unit is used where it is necessary to locate 2 panels for operations like welding.
- All parts should snap & butt properly to each other.
- Maintain a distance of 10mm to 12mm between the panel and other clamp parts.
- Avoid any clash to prevent issues at assembly.
Some main parts in Swivel clamp unit:
1. Finger /clamp mylar -
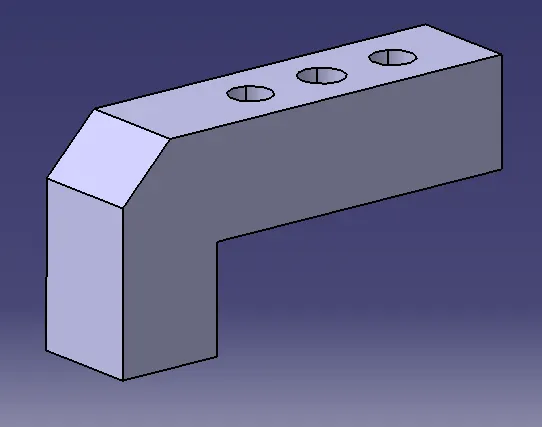
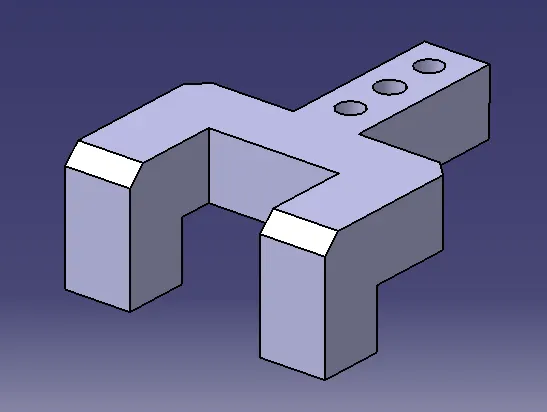
Fig shows: Clamp mylars
- It is a NC block mounted on the clamp arm of the cylinder.
- It is used for clamping / holding the car panel.
- It presses the car panel towards the rest.
2. Backup / Rest Mylar-
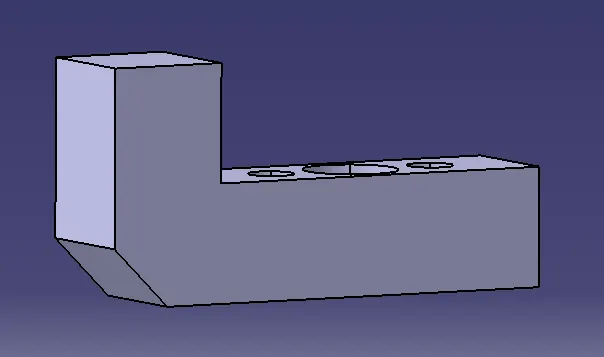
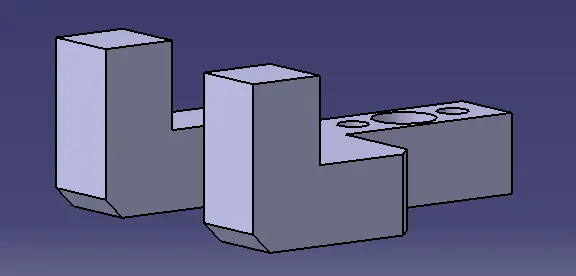
Fig shows: Rest mylars
- It is a NC block fixed to the unit to support the car panel.
- It helps in resisting the clamping force of cylinder onto the panel, thus clamping is achieved.
4. Clamp cylinder-
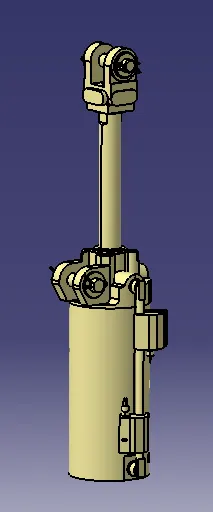
Fig shows: CKG_1B_63_100Y (Swivel clamp cylinder)
- Clamp cylinder is a pneumatic device which works with the flow of pressurised air.
- Clamp cylinder is a brought out part and some manufacturers are destaco, tuenkers, etc.,
5. Stopper-
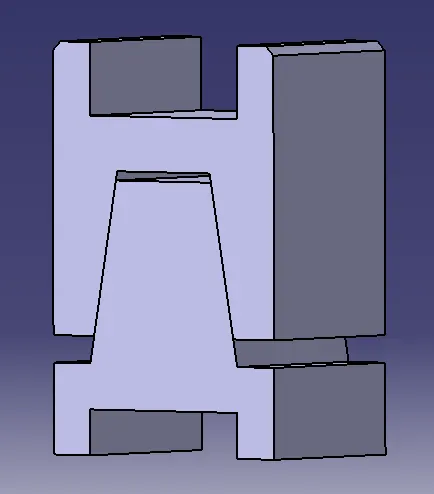
Fig shows: Stopper
- The main function of the stopper is to restrict the motion of the clamp arm beyond the blade or the limit.
- The stopper will be mounted between the clamp arm and the rest/blade.
Clamp-Pin unit:
- Pin unit is a unit designed to locate car panels using pins.
- It consists of riser, blade, block, pin retainer, pin, shims or spacers and cylinders(incase of retractable pin unit).
- Pin unit is a part of the 3-2-1 locating principle of fixture design.
- It restricts 6 degrees of freedom of the part.
- This is sometimes provided with the clamp unit when two panels are to be located for any operations like welding.
Fundamentals to be considered for pin design:
- Pin should engage at 3 to 5 mm from car panel entry surface.
- All pins should be accommodated with 2-way adjustable shims irrespective of direction of arresting.
- Round pins should be used incase of 4way arresting of car part if the hole is round.
- Round pins can be used for 2 way arresting of car parts only if the hole is slotted.
- Diamond pins should be used for 2 way arrresting of car part if the hole is round.
- Diamond pins should be used incase of 4 way arresting of car parts if the hole is slotted.
PURPOSE OF CLAMP UNIT AND REST UNIT
- The purpose of clamping tools is to securely hold the workpiece in position without obstructing the production process.
- It prevents the distortion during welding process and other processes.
- High clamping forces combined with compact dimensions are therfore the most important requirements for a clamping tool. For this reason, clamps are also equipped with mechanical transmission gear units.
DESIGN METHODOLOGY:
3-2-1 Principle achieved by clamping and resting:
- The 3-2-1 principle is the fundamental principle of all fixture design. While designing a fixture a major part of time is spent in locating the workpiece in the fixture.
- The best & the most effective method of part location is referred to as the 3-2-1 method. Fixtures work on the 3-2-1 principle.
- 3 locators or supports are placed under the workpiece which establishes the part plane. Three locators are generally positioned at the primary locating surface.
- This restricts 2 axial movements downward & upward and 4 radial movements. As a result the 3 locators arrest six degrees of freedom.
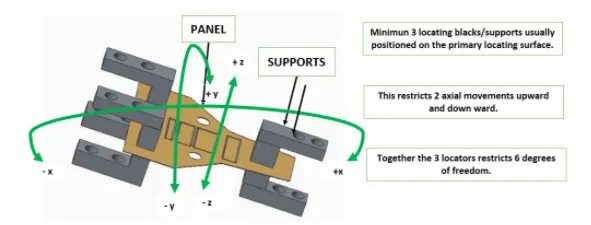
Fig shows: 6 DOF which are restricted by the locators or the clamps
- Thus by using 3-2-1 principle, introducing a minimum of 3 clamping & resting blocks will restrict 6 DOF( 2 axial translational about z-axis & 4 rotational about the x&y axes respectively).
- Remaining 6 DOF are restricted by introducing Pin unit of minimum 2 nos.
- Clamping- The process of holding the workpiece in the jig/ fixture is called clamping. The primary devices used for holding the workpieces are clamps/clamp unit.
- Resting - The car panel will rest on the rest unit. It resists the clamping force of the finger exerted by the clamp cylinder and thus clamps the car panel.
Forces acting in the clamp and rest unit:
while designing a clamp unit 2 forces are considered that act in clamp unit,
- Clamping force
- Holding force
1.Clamping force:
- It signifies the force applied to the workpiece by the drive mechanism via the clamp arm during gripping or clamping operations.
2. Holding force:
- Holding force, on the other hand denotes the maximum force after locking the knee-lever (over centre position, that can be applied by the workpiece on the gripper/clamp arm without destroying the mechanism.
- Therefore, particular attention must be paid to the maximum holding force when, for example during the production process (welding, bonding), there is a possibility of distortion of the component or if the clamp arm is used as a fixed stop.
- If the holding force specified in the technical details is exceeded, this will inevitably result in the destruction of the mechanism, the clamp arm or the bearing position.
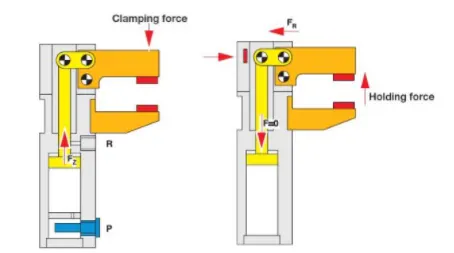
Fig shows: Clamping and holding forces
Design tree:
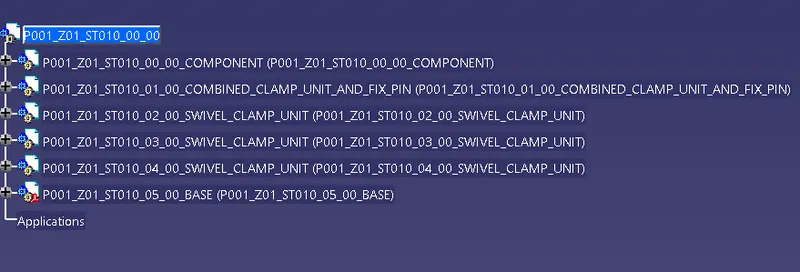
- It is the process of naming all the assemblies and parts in the specific standards. Different customers have different set of standards to structure a design tree.
- It is an important process which helps us to identify a specific part or assembly as to which project or assembly it belongs to.
- This helps us to avoid the errors during design study, manufacturing, assembly,inspection, etc.,
- If the parts or assemblies are not properly or the design tree is not structured properly, it will create confusion in understanding the design and assembly which may lead to errors.
- Naming of a fixture or a unit or a part gives their place in the specific project or assembly or zone.
- It helps us to identify the quantity of items of same type or different types that are being used in the assembly.
PLP Location and clamp plan:
PLP (Principle Locating Points):
- Principle locating points are the points that are used for the accurate location of the panels sub-assemblies to maintain the geometry of the assembly.
- There are lots of holes on the panel which are not accurate due to stamping operations. So the PLP are defined in the drawings.
- The PLP holes must be very much precise.
Clamp plan:
- It provides information of location of pins, clamp units, rest units,damp units.
- It is the important input from the customer end.
- The clamp plan/ position should not be changed without the knowledge of the customer.
- It is allowed to change the design little bit here and there but the input design data about the clamp position or pin location must not be changed.
- In clamp plan there is clamp unit,pin unit and it is more detailed. It also gives the Y and Z coordinates from where the designing process of fixture can be started.
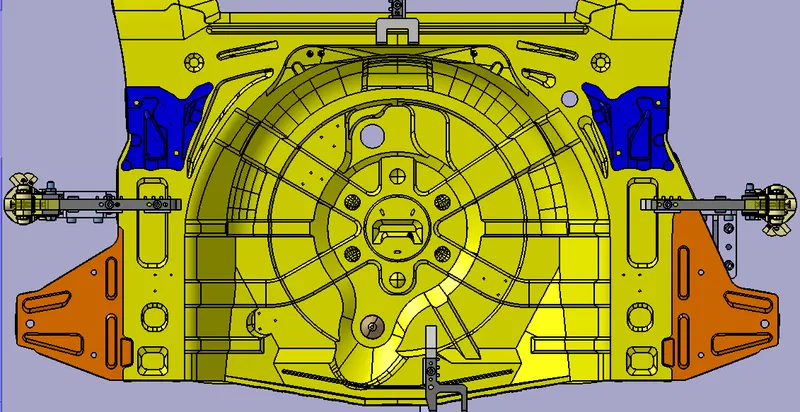
Fig shows: Clamp plan
Material used:
In general, the materials used for Mylars, Clamp arm, shims, block, blades & risers are:
- Mylars: UHMW, Nylon66, PP, Teflon (polytetrafluroethylene (PTFE). Materials of clamp block and rest block to be decided as per the A class panel or B class.
- Clamp arm: SAE 4140 or SAE 1045.
- Shims / Spacer: S.A.E. 1010 CRS FULL HARD, COLD ROLLED STRIP STEEL S.A.E. 1010 FULL HARD, S.A.E. 1020 HRS, etc.,
- Block: STEEL ASTM A-36, NM STAINLESS, STEEL ASTM A-36, SS type 303 or 304,etc.,
- Blade: STEEL ASTM A-36,etc.,
- Riser: STEEL ASTM A-36,etc.,
HARDNESS:
In general, the hardness of the materials for pins, pin retainers, shims, shim block, blades and risers are 55-60 HRC to a depth of 0.5-0.7 mm after grinding.
SURFACE FINISH:
In general, the surface finishes of the materials for pin, pin retainer, shims, shim block, blades and risers are:
- Clamp arm: Munsell No.3.75YR6/14 safety orange.
- Shims/spacers: BLACK OXIDE FINISH (SURFACES TO BE FLAT AND PARALLEL TO WITHIN 0.012 mm T.I.R.)
- Riser: SURFACES TO BE FLAT, PARALLEL & PERPENDICULAR TO WITHIN 0.015 T.I.R.
Images of the DESIGN
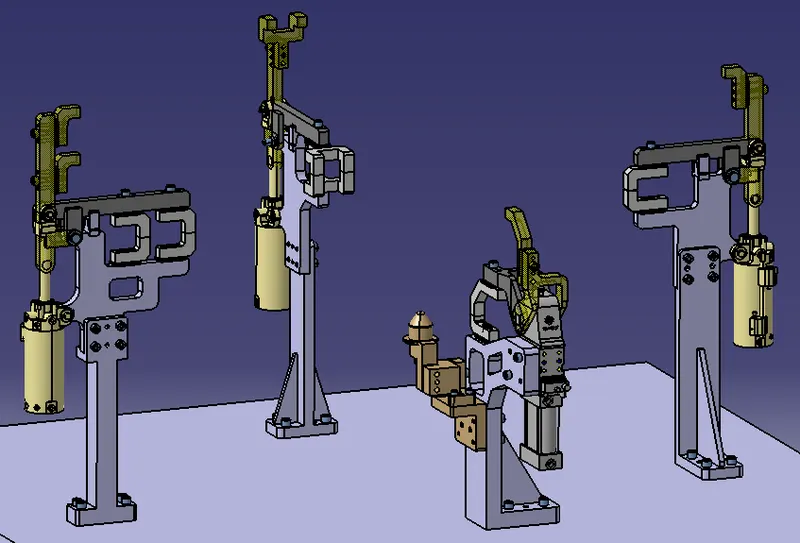
Fig shows: Positions of clamp units on the base
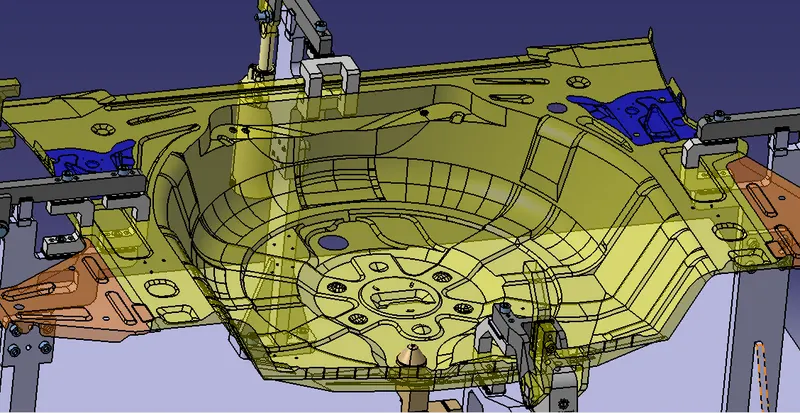
Fig shows: Assembly of swivel clamp units(a)
Fig shows: Assembly of swivel clamp units(b)
CONCLUSION
Hence as per the objective, design of 3 Swivel clamp units with different riser, blades, clamp arm, mylars, stopper is done by considering clamping and holding forces. The design of a clamp-pin unit is also done with the use of power clamp units.