Week 2:- BiW Fixture Basics Challenge
1. What is the process of project execution activity?
Answer:
Project execution is the stage of the project where everything has been planned is put into action. The main objectives are:
- To keep the work on track
- To organize team members
- To manage timelines
- To make sure the work is being done according to the original plan.
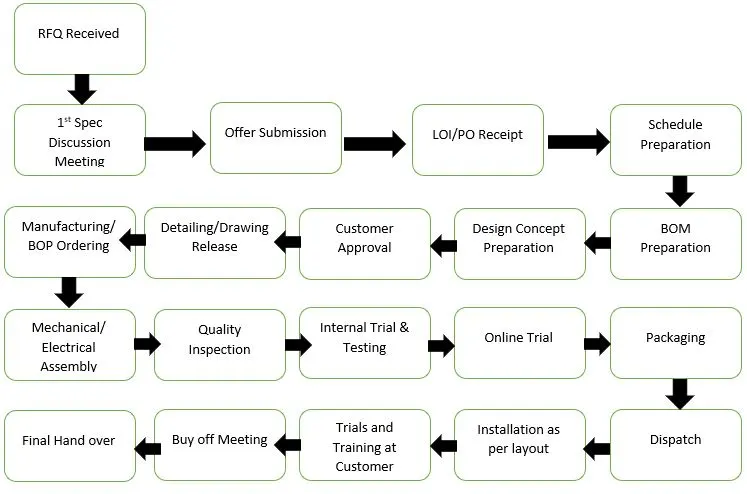
1. RFQ:
- Request For Quotation (RFQ) is the first step involved in project execution phase.
- In this activity the customer quotes his/her recquirements and specifications regarding the project in a detailed document.
- Besides the technical offer, commercial offer, expected timeline of the project and oether details are also provided.
2. First spec discussion meeting:
- After the RFQ is received, there will be a discussion meeting about the technical offer, commercial offer, project execution, timeline recquired to complete the project and the crew will make a final decision based on the result.
- In addition, the time required to complete the project from the begining of data study,3d concept design, simulation validation, quality check,2D drawing release,manufacturing,etc., are calculated and prepared in the technical offer.
- Based on technical offer commercial offer will be finalized.
3. Offer submission:
- After the finilization the offer is submitted to the customer end.
- The customer will also receive more offers from other companies. The customer will go through the offers and analyse it.
4. LOI/PO receipt:
- After the customer has analysed the offers in all aspects, the final LOI/PO (Purchase Order) will be issued to the respective manufacturer end.
- Once the PO is received the project work has to be started by preparing schedules.
5. Schedule preparation:
- After receiving the PO, the project schedule preparation will be done to meet the project deadlines specified by the customer in order to complete the project.
- All the stages in the project are considered for the calculation of time recquired to complete the actions such as kick-off meeting, design data study, DAP, simulate quality check, 2D detailing, drawing check, release of BOM, manufacturing, boughts out of electrical and mechanical components, assembly of fixture, paints,etc.,
- The above mentioned activities are traced in the schedule preparation chart.
- If the date obtained does not match with the dead lines, then the schedule is revised accordingly and meetings are held.
6. BOM preparation:
- Bill of materials like cylinders, motors,bolts, nuts,etc., are listed and prepared.
7. Design concept preparation:
- Before this step a complete study of design data is done as per the customer recquirements.
- During the design data study activities some rough sketches are done to get the flow of design.
- It undergoes conceptualization of basic data like spot plan,cycle time,etc.,
- To avoid collision of weld guns with the clamps while traveling, spot plan is made in the initial stage.
8. Customer approval:
- In this step the customer reviews the design data and checks whether the design fulfills the recquirements of the proposed design or not based on the technical offer.
- If it is ok then the customer will finalize the approval and if it is not ok, several steps are to be taken to re examine the schedule and design. After that the result must be submitted for approval.
9. Detailing and drawing release:
- Once the customer approved the project, the detailed drawings and designs are prepared at the manufacturer end.
- It is released for all the parts recquired with the appropriate dimensions,tolerances,quantity,specifications,etc.,
10. Manufacturing/BOP ordering:
- In this stage the recquired components for manufacturing like motors,cylinders,sensors,gripper,etc., are ordered as per the specifications recquired.
11. Mechanical/ Electrical assembly:
- After all the parts from the BOP ordering are received, they are subjected to quality check by the quality department with respect to the specifications.
- Then the mechanical and electrical parts are assembled.
12. Quality inspection:
- Quality checking is again done once after the assembly is finished.
- The dimensions, positional accuracy, coordinates are checked by using CMM machine.
- Only the approved assembly is passed to the next level, rest is sent back to the assembly for re-assembly work.
13. Internal trial& testing:
- The next to quality check is the internal trial which is done to evaluate the operation of the fixture.
- It is the inhouse testing where the seating of the assembly/panel, clamping,postion of pins into holes are checked for proper outcome.
14. Online trial:
- It is done in automated mode by using electrical connections.The process sequence is checked as per the designed way in front of the customer for further approval.
15. Packaging:
- It is done to avoid damage during transportation which may affect the proper function and aesthetic look of the fixture.
- Hence proper packaging is done to ensure the geometry of the fixture.
16. Dispatch:
- After the fixture has been properly packed, it will be dipatched to the customer end with the mentioned address.
17. Installation as per layout:
- At the initial stage itself the layout for the fixture assembly is prepared which defines the space for the robots,fixture,etc.,
- The layout is prepared by considering the functionality,application, process sequence,etc., Hence the installation is to be done as per the layout.
18. Trials and training at customer:
- Production trials will be carried out at the customers end. As the technical offer defines the 'n' number of assemblies will be completed in 8hrs/ 12hrs shift.
- So the production trial is carried out to ensure the capability of the fixture as per the technical offer terms.
- Once it is achieved, training will be provided to the workers, engineers, operators about handling the fixture like loading, unloading of the part,etc., also the sequence of process will be explained.
19. Buy off meeting:
- In this meeting the customer reviews are taken and in some cases the customer may ask for some additional features to be included in the fixture.
- Those requests are analysed and finalized by conducting meetings.
- All the doubts from the customer end are clarified and process is moved further.
20. Final handover:
- In this step, the product is finally handed over to the customer.
- The documents like clamp validation document, ergo sheets, BOMs,etc., will also be handed over to the customer along with the fixture.
- We can carry a proof for our work done as documents.
- Every automobile industries will follow some document standards like ISO & IATF.
- IATF(International Automotive Task Force) is a group which is followed by most industries now-a-days.
2. What are the types of joining processes?
Answer:
JOINING PROCESS
Joining process is the process of joining two metal parts(similar or dissimilar) either temporarily or permanently with or without the aid of heat or pressure.
There are 3 types:
- Mechanical joining
- Metallurgical joining
- chemical joining
1. MECHANICAL JOINING
- Mechanical joining is the process of joining parts using mechanical methods which makes use of screws,nuts,bolts,rivets,shrink fitting,etc.,
- The threaded holes employed for mechanical joining are vulnerbale to fracture.
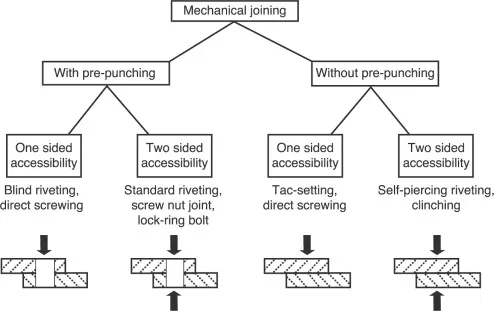
- As shown in the figure mechanical joining is classified as joints with pre-punching and joints without pre-punching. Punching is nothing but drilling.
- In case of joints with pre-drilling, there will be holes with thread through which the bolts and nuts are used to join the parts. In this both the nut and bolt can be accesssed from either sides.
- In case of joints without pre-drilling, there will be no holes where the riveting is carried out. Riveting is done by piercing through the metal part and only one side of the rivet is accessible.
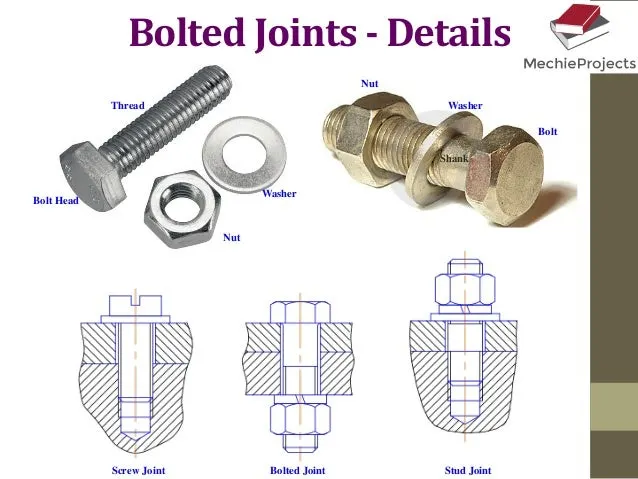
I. Bolt and screw:
- It is a temporary joint made using bolts and nuts or screws. This is widely used in assembling of parts which are to be temporarily joined or recquire periodic maintenance.
- There are 2 types : TENSION JOINTS and SHEAR JOINTS.
II. Self peircing riveting
- It is a high speed mechanical fastening process that instantly makes the joints in point joining sheet material, typical material, aluminium alloys.
- It is a single step technique generally uses a semi tubular rivet to clinch the sheet in the mechanical joint.
- Pre-drilling holes are not required since it is self peircing joint made in one rapid operation.
FIG SHOWS: A common rivet joint
III. Hemming and Seaming process:
- Hemming and seaming are 2 similar metal working processes in which a sheet metal is rolled over onto itself.
- Hemming is a process in which the edge is rolled flush to itself whereas seaming is the process of joining the edges of 2 materials.
Fig shows: Different methods oh hemming
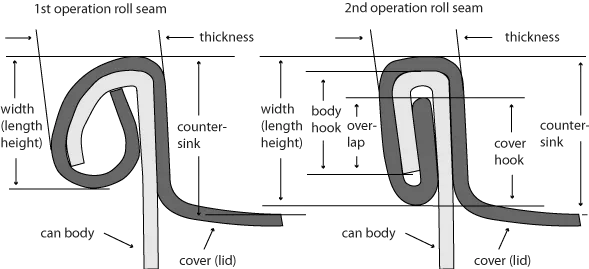
Fig shows: Seaming process
2. Metallurgical joining:
- It joins two metals involving metallurgical changes in it.
- In some cases the metals are fused or heated or a filler material may be used,etc.,
- Mainly classified as: Welding, brazing, soldering, diffusion bonding,etc.,
I. WELDING
- Welding is a fabrication process that joins materials, usually metals or thermoplastics, by using high heat to melt the parts together and allowing them to cool, causing fusion.
- Welding is distinct from lower temperature metal-joining techniques such as brazing and soldering, which do not melt the base metal.
Fig shows: Welding of metals
- Types of welding:
- Fusion welding
- Electric resistance welding
- Solid state welding
a. Fusion welding
- In this type of welding the metal at the joint is heated to the molten state and it is allowed to solidify.
- Filler material may be needed for some kind of metal joints.
- It is classified as thermit welding, arc welding and gas welding.
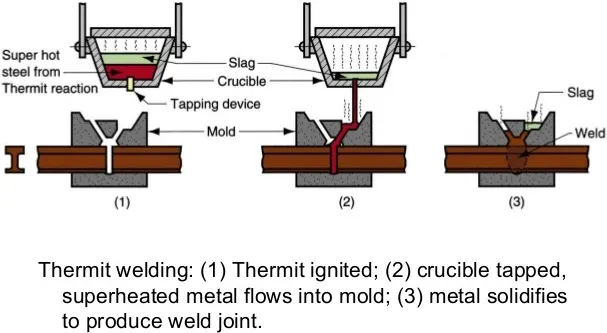
- Thermit welding - It is welding of parts by using liquid thermit steel around the portions to be welded. Since its a fusion welding process, neither arc is produced to heat the parts nor flames are used. For getting high temperature the exothermic reaction is used.
- Welding principle is the heat of the thermit reaction used for welding in plastic states and mechanical pressure is applied for the joint.
- Arc welding- In arc welding process heat is developed by an electric arc. The electric arc is produced between the electrode and the workpiece.
- It is a process of joining 2 metal pieces by melting their edges by an electric arc.
- In arc welding electrical energy is converted into heat energy.
- The gap between the electrode and the workpiece is maintained at 3mm approx. Then current is supplied which produces the electric arc.
- The workpiece and the electrode is melted and both the parts will become a single piece without applying any external pressure.
- The temperature of arc is about 5000°C to 6000°C.
- A filler material is introduced during the welding which deposits along the weld bed.
- The depth to which the metal is melted and deposited is called the depth of fusion. To obtain a better depth of fusion, the electrode is kept at an inclination of 70° to the vertical.
- Types of arc welding:
- Manual Metal Arc Welding
- MIG
- TIG
- Submerged Arc Welding
- Plasma Arc Welding
- Atomic Hydrogen Arc Welding
- Carbon Arc Welding
- Eletroslag Welding
Fig shows: Shielded Metal Arc Welding (SMAW)
b. Electric resistance welding
- Resistance welding is one of the most commonly used welding techniques in the manufacturing industries for joining metal sheets and components.
- It is mostly employed in the BIW assemblies.
- Here, the weld is made by conducting a strong current through the metal combination to heat up and finally melt the metals at the localized points predetermined by the design of electrode or the workpiece.
- A force is always applied beefore,during and after the application of cuurent to confine the contact area at the weld interface and in some cases to forge the sheets.
- Types of resistance welding:
- Resistance Spot Welding
- Resistance Seam welding
- Resistance Projection welding
- Butt welding
- Precursion welding
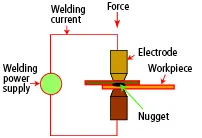
Fig shows: Resistance Spot welding
c. Solid state welding
- Solid state welding is the welding process in which the two workpieces are joined under the pressure providing intimate contact between them and at a temperature essentially below the melting point of the parent material.
- Bonding of the material is a result of the diffusion of their interface atoms.
- Classified as:
- Forge welding
- Cold welding
- Friction welding
- Explosive welding
- Diffusion welding
- Ultrasonic welding
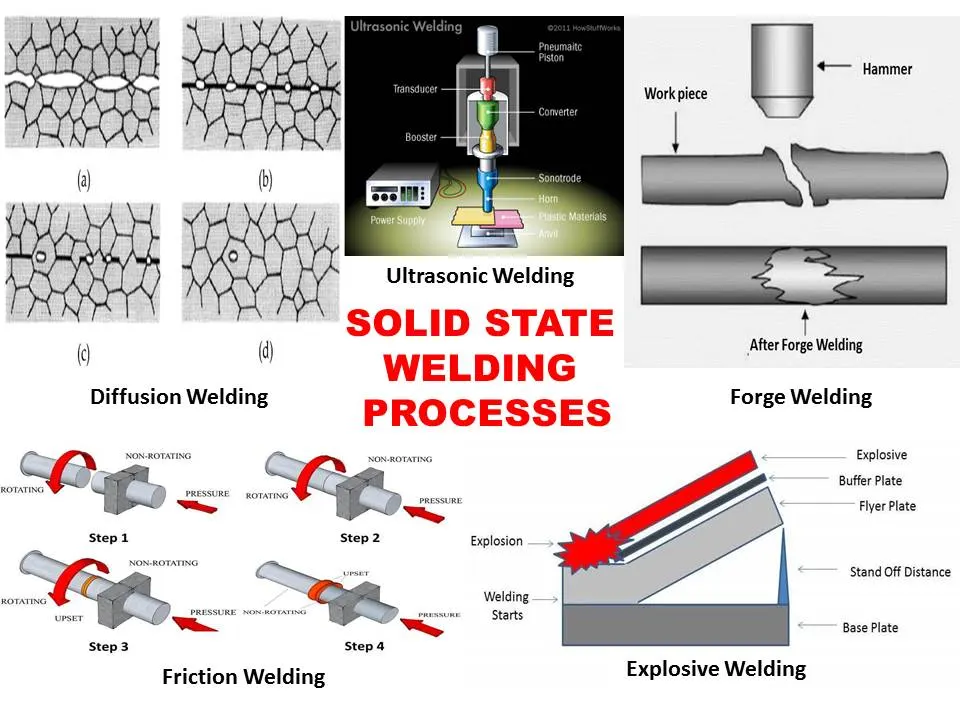
Fig shows: Types of solid state welding
II. BRAZING
- In brazing 2 workpieces are joined together using a filler material that is spread between them.
- The filler material alone is melted withough causing any melting in the workpieces.
- The temperature for brazing should be high enough to melt the filler material but less for the workpiece.The material used as filler material should melt above 450° C.
- Flux is also used in brazing to eliminate the oxides on the surface which prevents oxidation.
- This will ensure a good metallurgical bond between the filler and workpiece.
- Once melted, the filler material fills up the spaces between the workpieces to be joined and even manages to fill the tight gaps by capillary action. Then it is cooled down to get a strong bond.
III. SOLDERING
- Soldering is a joining process used to join different types of metals together by melting solder.
- Solder is a metal alloy usually made of tin and lead which is melted using a hot iron. The iron is heated to temperatures above 600° fahrenheit which then cools to create a strong electrical bond.
- Brazing material are those that melt above 450°C,so the soldering material are those that melts at 450°C.
- Like welding and brazing soldering also includes flux material to clean up the surface to be soldered and improves the metallurgical bond. Residues from the fluxes, however must be removed aftering soldering to prevent corrosion.
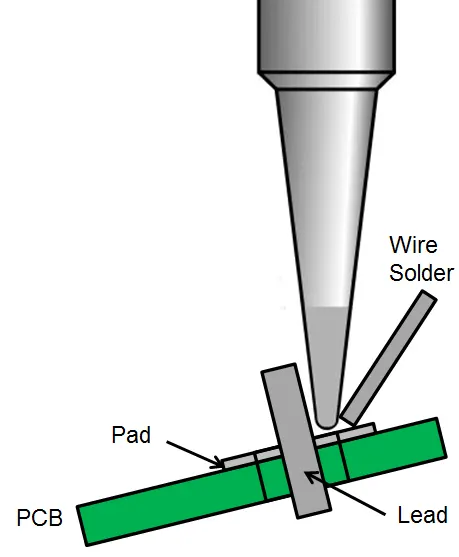
Fig shows: Soldering
3. Adhesive bonding:
- Adhesive Bonding is the process of joining two surfaces together, usually with the creation of a smooth bond.
- This may involve the use of glue, epoxy, or one of a wide range of plastic agents which bond either through the evaporation of a solvent or through curing via heat, time, or pressure.
- It uses bonding chemicals or materials known as adhesives.
- It is used to join polymers and polymer-matrix composites, polymers to metals, metals to metals and ceramics to metals.
- It can withstand shear, tensile and compressive stresses but they donot have good resistance over peeling.
- One of the main advantages of adhesive bonding is that it allows for the even distribution of stress loads, thereby reducing the stress on the joint. Since they are applied inside the join, adhesives are also invisible within the assembly.
- To improve the adhesive bonding, the surface of the adherent must be cleaned thoroughly to remove the dust and interfacial gaps between the adhesive and adherent.
- Rough surfaces also improves the adhesive bonding strength since they provide better mechanical interlocking.
Fig shows: Adhesive bonding
3. What is resistance welding and its application in automotive sector?
Answer:
RESISTANCE WELDING
- Resistance welding is one of the most commonly used welding techniques in the manufacturing industries for joining metal sheets and components.
- It is mostly employed in the BIW assemblies.Here, the weld is made by conducting a strong current through the metal combination to heat up and finally melt the metals at the localized points predetermined by the design of electrode or the workpiece.
- A force is always applied beefore,during and after the application of cuurent to confine the contact area at the weld interface and in some cases to forge the sheets.
- Types of resistance welding:
- Resistance Spot Welding
- Resistance Seam welding
- Resistance Projection welding
- Butt welding
- Precursion welding
Fig shows: Classification of Resistance Welding
1. RESISTANCE SPOT WELDING
- The process is used for joining sheet materials and uses shaped copper-chromium or zinc-chromium alloy to apply the pressure and supply electric current through the workpiece.
- Heat is developed mainly at the interface causing the metal to melt at the localized point forming a molten pool which is called as weld nugget.
- The molten pool is contained by the electrode and the surrounding solid metal which on cooling makes a strong bond.
- They are done at spots. These spots are first specified at intervals along the workpiece.
Fig shows: Resistance Spot welding
- Application of resistance spot welding:
- The most common application is the automobile industries where it is used universally to weld the sheet metal to a car.
- Resistance spot welding has short weld time and hence high weld speed. Hence it is adaptable to automation and robotics.
- Typical Biw contains 5000 welds. The strength depends on the RSW.
- Skilled workers such as dentists also use spot welding in orthodontics field.
- Besides this, fabrication and repair shots extensively use spot welding.
2. RESISTANCE SEAM WELDING
- Resistance seam welding is a variant of the basic resistance spot welding process. In spot welding a weld nugget is produced by passing an electric current through the sheet materials to be welded.
- In seam welding a series of overlapping nuggets is produced, usually by replacing the conventional spot welding electrodes by wheels that turn as the parts to be welded are fed between them. The process thus produces a continuous leaktight seam.
- It is the joining of work pieces made of similar or dissimilar materials along a continuous seam. Seam welding can be broken down into two main techniques, resistance seam welding and friction seam welding.
- It is used for closed and no gap parts.
- The current and heat generation are localized by the peripheral shapes of the electrode wheels.
Fig shows: Resistance Seam Welding
- Applications of resistance seam welding:
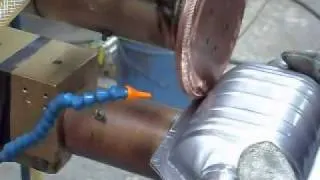
Fig shows: Seam welding of a leak tight can.
- It is mainly used for the welding of air tight tanks or compartments.
- It can be used to make gas- or fluid-tight joints in a variety of sheet metal fabrications.
- Steel fuel tanks for motor vehicles are a prime example. It is also used in making tin cans, steel drums and domestic radiators.
- It is also used in the fabrication of heat exchanger.
- It is used to weld leak proof beverages, home utensils, water sinks, radiators,etc.,
3. RESISTANCE PROJECTION WELDING:
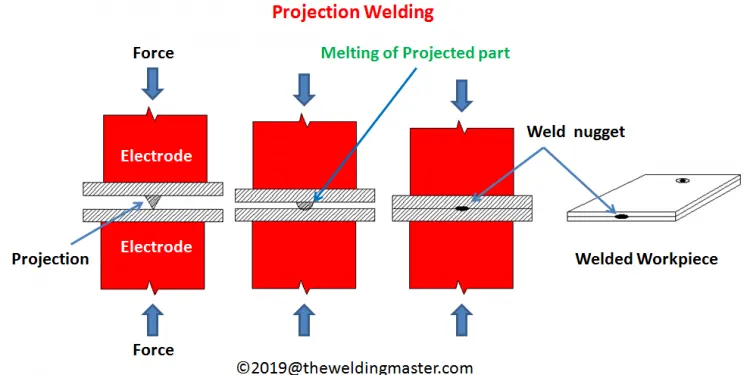
Fig shows: Projection welding process
- Resistance projection welding, or RPW, is a form of resistance welding where the electricity, force, and time are concentrated on raised segments (projections) to join items together.
- It is similar to the resistance spot welding where the localization of the ppoint is defined by the shape of the workpiece either with their natural shape or a specially designed projection.
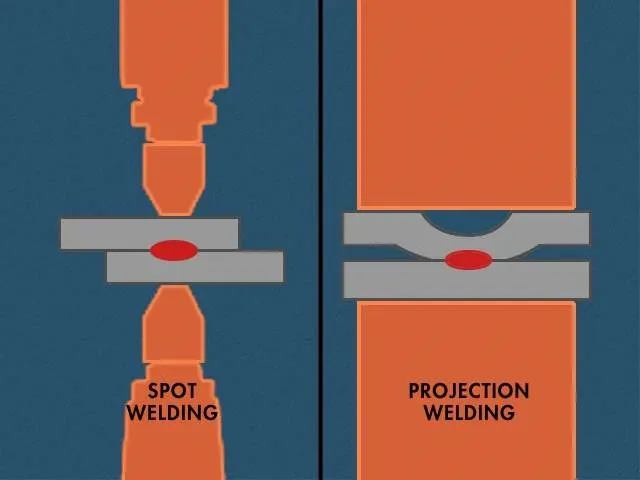
Fig shows: Difference between projection and spot welding
- Since the only contact point between the workpieces are the projections, current passes through the projection and it melts the metal under pressure which confines the molten pool.
- After cooling the result is several weld nuggets holding the part together. Of course in the case of cross wire welding there is one weld per crossing location but normally many are welded at the same time as in fencing.
- Applications:
- It is used in door assembly and in some special parts in the BIW structure.
- It is widely used in automobile industries, where screw-fastener parts such as nuts and studs are joined to metal sheet components.
- It is also found in cross wire and bar welding, or in day to day products such as shopping carts.
- It is used in refrigeration works like mass production of condensers, gratings, racks, etc.,.
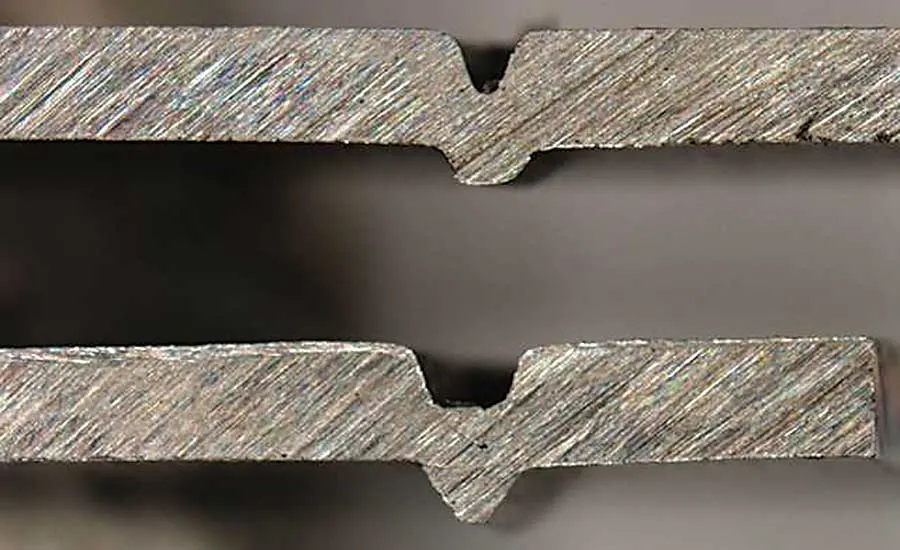
Fig shows: An application of projection welding
4. What is fusion welding and types of fusion welding with its application in the automotive sector?
Answer:
Fusion welding
- In this type of welding the metal at the joint is heated to the molten state and it is allowed to solidify.
- Filler material may be needed for some kind of metal joints.
- It is classified as -
- Thermit welding
- Arc welding
- Gas welding.
1. Thermit welding:
- It is welding of parts by using liquid thermit steel around the portions to be welded. Since its a fusion welding process, neither arc is produced to heat the parts nor flames are used. For getting high temperature the exothermic reaction is used.
- Welding principle is the heat of the thermit reaction used for welding in plastic states and mechanical pressure is applied for the joint.
2. Arc welding:
- In arc welding process heat is developed by an electric arc. The electric arc is produced between the electrode and the workpiece.
- It is a process of joining 2 metal pieces by melting their edges by an electric arc.
- In arc welding electrical energy is converted into heat energy.
- The gap between the electrode and the workpiece is maintained at 3mm approx. Then current is supplied which produces the electric arc.
- The workpiece and the electrode is melted and both the parts will become a single piece without applying any external pressure.
- The temperature of arc is about 5000°C to 6000°C.
- A filler material is introduced during the welding which deposits along the weld bed.
- The depth to which the metal is melted and deposited is called the depth of fusion. To obtain a better depth of fusion, the electrode is kept at an inclination of 70° to the vertical.
- Types of arc welding:
- Manual Metal Arc Welding
- MIG
- TIG
- Submerged Arc Welding
- Plasma Arc Welding
- Atomic Hydrogen Arc Welding
- Carbon Arc Welding
- Eletroslag Welding
a. Manual Metal Arc Welding/ Shielded Metal Arc Welding:
Fig shows: Shielded Metal Arc Welding (SMAW)
- Manual Metal Arc Welding (MMAW/MMA) also known as Shielded Metal Arc Welding (SMAW) and informally known as stick welding.
- Stick welding is a process where the arc is struck between the metal rod (electrode flux coated) and the workpiece, both the rod and the workpiece melts to form the weld.
- An electric current either AC/DC is used as electric power supply.
- That power supply is used to form an electric arc between the electrode and the workpieces.
- The workpiece and electrode melts to form a molten pool which solidifies then to form the joint.
- As the weld is laid, the flux coating of the electrode provides the shielding gas as a layer of slag. These protects the weld area from atmospheric contamination.
- It is used in the joining of base parts of chasis and doors of the automobiles.
b. MIG welding:
- MIG welding - Metal Inert Gas welding.
- It is an arc welding technique in which a consumable electrode is used to weld 2 or more workpieces.
- It makes use of following components:
- Consumable electrode
- Inert gas supply
- Welding head
- AC/DC power supply
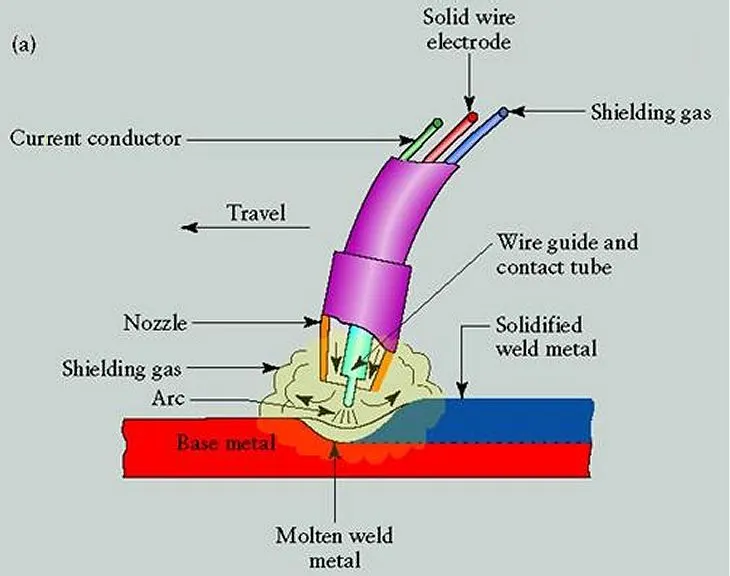
Fig shows: MIG welding
- It is also known as Gas Metal Arc Welding or Metal Active Gas Welding.
- The process can be semi-automatic or automatic.
- A constant voltage, DC power source is mostly used with GMAW, but constant curent systems as well as AC, can be used.
- There are 4 primary methods of metal transfer in GMAW, namely globular, short-circuiting, spray and pulsed spray each of which has distinct properties and corresponding advantages and limitations.
- This welding is used in the joining of bone, chassis area and engine part in automotive industry.
c. TIG:
- TIG - Tungsten Inert Gas Welding.
- It is an arc welding technique that uses a non-consumeable electrode tungsten electrode to weld 2 or more workpieces.
- The following components are required to perform TIG welding. They are:
- Power supply
- Non-consumeable tungsten electrodes
- Inert gas supply
- Filler rod(depends on nature of workpiece)
- Welding head
Fig shows: TIG welding
- An inert shielding gas is used to protect from oxidation or other atmospheric contamination.
- A constant current welding power supply produces electrical energy, which is conducted across the arc through a column of highly ionized gas and metal vapors known as plasma.
- TIG welding is most commonly used to weld thin sections of stainless steel and non-ferrous metals such as aluminium BIW structures of automobile.
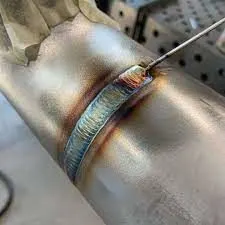
Fig shows: Application of TIG welding
3. Gas welding:
- Gas welding is one type of welding process in which the edges of the metals to be welded are melted by using a gas flame.
- NO pressure is applied during welding except pressure gas welding.
- The flame is produced at the tip of the welding torch.
- The gases commonly used are acetylene, hydrogen,propane and butane.
- It is used to weld the metal parts with thickness at the range of 2mm to 50mm.
- There are 3 types of welding processes that are employed in industries,
- Oxy-acetylene welding
- Oxy-hydrogen welding
- Air-acetylene welding
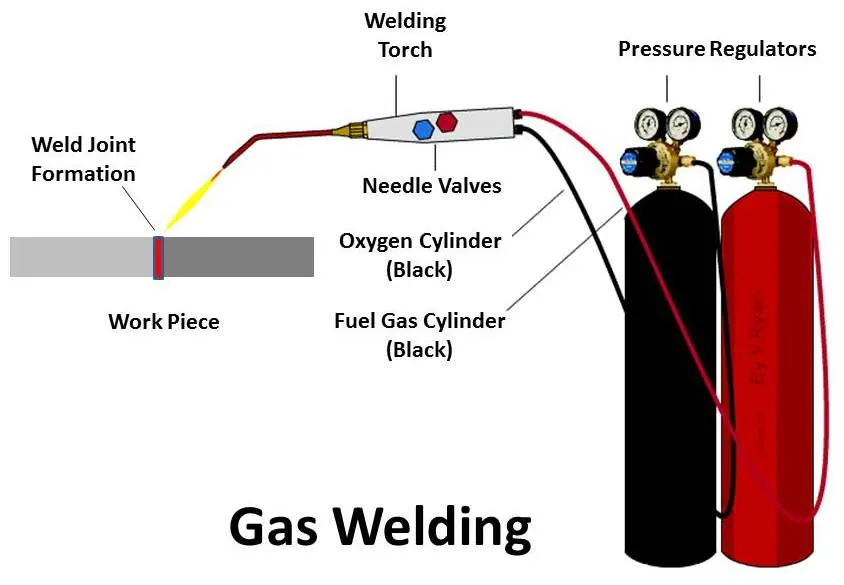
Fig shows: Gas Welding setup
- The most commonly used welding is the Oxyacetylene welding.
- Oxyacetylene welding- In this welding, the heat is obtained by burning a mixture of oxygen and combustible gases. The gases are mixed in the required proportion in a welding torch which provides the control of the welding flame.
- The flame only will melt the metal and a filler rod is used to fill the gap.
- Flux is used to prevent oxidation and to remove impurities.
- The temperature at the hottest region is about 3200°C.
- The cost of acetylene is low. The gases O2, C2&H2 can be stored at high pressure in separate tanks. But the acetylene is vey harmful if it is not handled carefully.
- There are two systems like High pressure system and low pressure system.
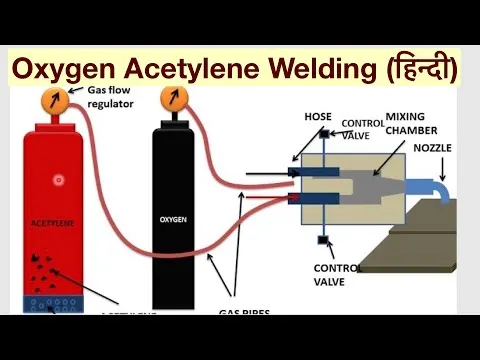
Fig shows : Oxyacetylene welding
5. What is 3-2-1 principle?
Answer:
3-2-1 Principle
- During metal working process it is very much important to locate the workpiece to be worked with respect to the fixtures.
- The accuracy with which a part is machined is quite dependent on the accuracy with which it is positioned in the fixture.
- Any variation in part location on the fixture adds to the dimensional tolerance that must be assigned to the finished parts.
-
This is true because improper supporting or clamping can temporarily or permanently deform the part.
- The method of supporting and securing the part in the fixture affects not only dimensional tolerances, but also surface finishes.
- Techniques for supporting and clamping must be considered together with the method of locating in order to assure repeatability from part-to-part.
- The basic principle of fixture is to restrict all degrees of freedom in the desired location and orientation.
- Locating of a part to be machined is a three-step process:
1. Supporting
2. Locating (positioning)
3. Holding (clamping)
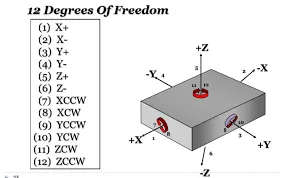
Fig shows: Degrees of freedom for a body in space
- The 3-2-1 principle is the fundamental principle of all fixture design. While designing a fixture a major part of time is spent in locating the workpiece in the fixture.
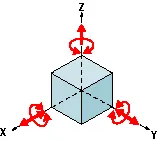
- Generally, a free body has 12 DOF(degrees of freedom):
- 6 Translational DOF
- 6 Rotational DOF
Translational DOF includes:
+X, -X, +Y, -Y, +Z,-Z
Rotational DOF includes:
- Clockwise around X axis (XCW/CROT-X)
- Counter or anticlockwise around X axis (XCCW/ACROT-X)
- Clockwise around Y axis (YCW/ CROT-Y)
- Counter clockwise /anti clockwise around Y axis (YCCW/ACROT- Y)
- Clockwise around Z axis (ZCW/CROT-Z)
- Counter clockwise around Z axis (ZCCW/ACROT-Z)
For proper fixing of parts one should restrict all 12 DOF of the workpiece. This is achieved by provoding 6 locating points, 3 pins in base plane, 2 pins in vertical plane and 1 pin in a plane which is perpendicular to the first 2 planes.
- Without 3-2-1 principle it’s very difficult for the BIW product engineer, BIW process engineer or BIW fixture design engineers to have same clamping and location scheme.
- Any geometry is fixed or hold in position with the 3-2-1 principle. To restrict it transverse motion in X, Y and Z direction and rotational movement in X,Yand Z direction object will be held in position with 3-2-1 principle.
- For e.g.: Consider a solid cube lying on a XY Plane and Z is height.
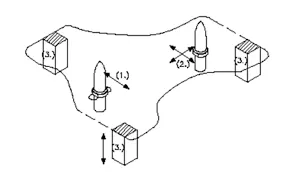
- 3 Points in Z direction defines the plane and restrict it movement along Z and rotation along X and Y.
- 2 Points in X direction restrict its movement in X and rotation along Z.
- 1 Point in Y restricts its movement in Y.
- This fundamental is used during the automotive body component design and welding tool design for its manufacturing.
Locating Process:
First plane-
- This is the "3" in 3-2-1. So, three specific points are used to define the first plane.
- Fewer than three points cannot define a plane, and in the real world dimensional tolerances mean that four or more points will not be coplanar. A real-world, less than ideally perfect part placed on four or more reference points will, in fact, rest on only three of the points due to its less than perfect surface.
- Different parts may rest on different combinations of three points, resulting in variation between finished parts. A stool can be used to illustrate this concept.
- A two-legged stool would certainly be unstable. A three-legged stool sits rock-solid. A four-legged stool is often found to rock. In the illustration, a three dimensional part, represented by a cube, is placed on a datum plane defined by three support points.
- TIPS
- Use the largest surface of the part for the first ("primary") reference plane.
- Position the three support points as far apart as possible.
- If more than three support points are required to prevent deflection, make the additional points adjustable.
Second plane -
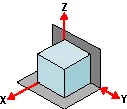
- A second plane, if it is perpendicular to the first, can be defined by two points, the "2" in 3-2-1.
- The part is now constrained to one degree of freedom: movement along the Y axis. (The part cannot move along the X or Z axes because it is held against the planes by clamping force.)
- TIPS
- Use the largest surface of the part for the first ("primary") reference plane.
- Position the three support points as far apart as possible.
- If more than three support points are required to prevent deflection, make the additional points adjustable.
Third plane -
- A third plane, if it is perpendicular to both of the first two planes, can be defined by one point, the "1" in 3-2-1. The part is now entirely constrained.
- It cannot move along or rotate about the X, Y, or Z axes. (Remember that the part is held against each of the three planes by clamping force.)
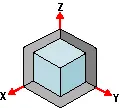
- TIPS - If more than one support point is required to prevent deflection, make the additional points adjustable.
6. Define Body Coordinate System.
Answer:
BODY COORDINATE SYSTEM
- The body coordinate system is widely used in the automotive industry for drawing of body parts, products and process design.
- A coordinate system is a reference system consisting of a set of points,lines and surfaces,used to define the positions of points in space in either two or three dimensions.
- In general BCS is also called as car line and body line.
- Maintaining X, Y & Z coordinates in fixture is a very important factor. We should try that the co-ordinates of locating and clamping points should not be in three decimal. (e.g.X=100.124, Y=245.127, Z=450.458)
- They should be whole nos. or maximum upto 1 decimal. Once these co-ordinates are maintained automatically the BIW base structure is maintained.
X = Longitudinal direction[(Fore and After- F/A) or (Front O Line- FOL)]
Y = Transverse direction[(Cross car- C/C) or (Centre O Line- COL)]
Z = Vertical direction[(Up and Down- U/D) or (Bottom O Line- BOL)
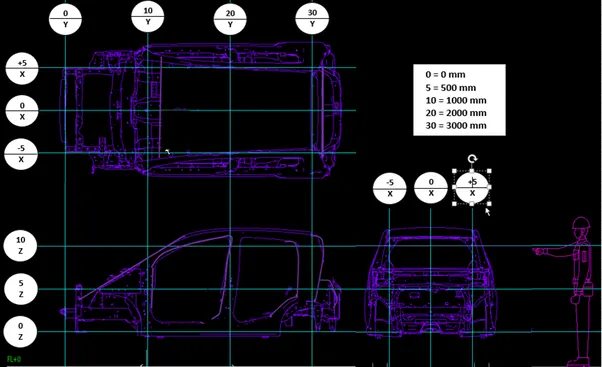
Fig shows: Body co-ordinate system
X(width of BIW) - OX is Body Center Line
Y(length of BIW) - OY is Near Front Bumper
Z(Height of BIW) - OZ is about Center of Wheel
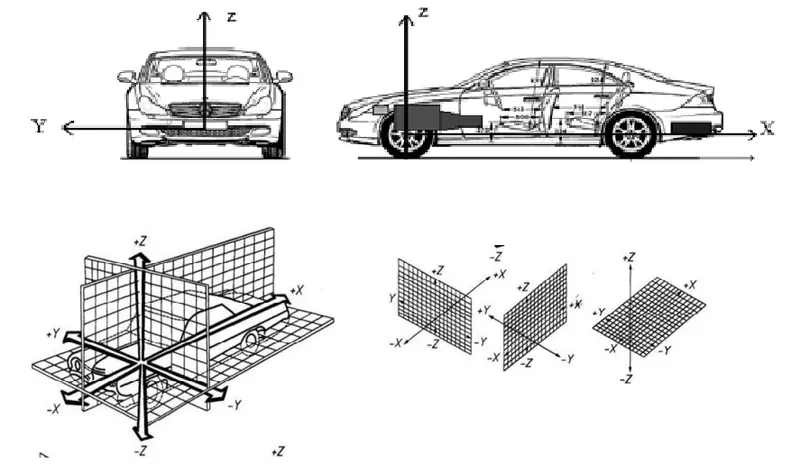
Fig shows: Body Coordinate System
- The above schematic figure shows the basic car geometry system used widely to specify the position of parts which is to be assembled to the car body. From the first part of the production line this coordinate system is used to specify its position.
- According to the CAD data some references are specified to the car body on the basis of which each and every part of the car body is assembled respectively.
- The fixture position is also defined with reference of these coordinate system. The fixture is installed on the basis of these reference point defined by CAD data according to which the fixture base plate and the accessories are installed..
- Each and every parts measurement is done with reference to this coordinate system. The deviation in the assembly of car body and the components is shown with respect to these coordinates. An individual part measurement is also done with respect to these coordinate system.
- Accuracy of the BIW is also defined by the final measurement report which are based on these coordinate system.
7. Elaborate Body Plane System & its essentials.
Answer:
BODY PLANE SYSTEM
- Body planes are reference planes in an automotive car. These planes are used to define the GD&T of all parts in an automotive domain.
- Body planes are 3 mutually perpendicular imaginary planes.
- The measurement from body plane to parts are called body plane dimensions.
- The planes are generally considered to be present in the driver position or sometimes at engine location or at the front end of the car depending on the customer.
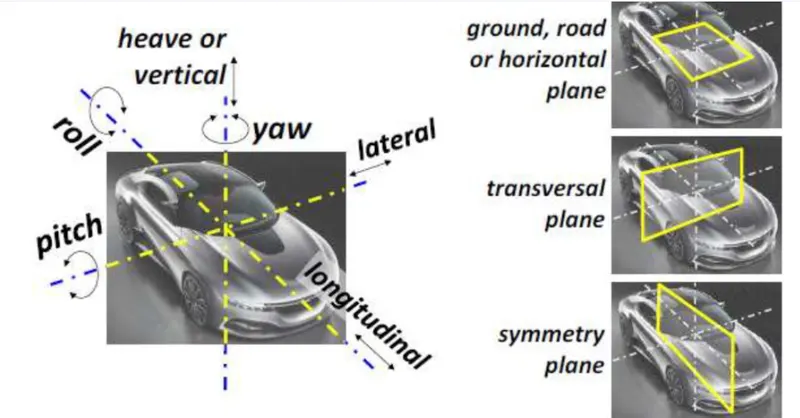
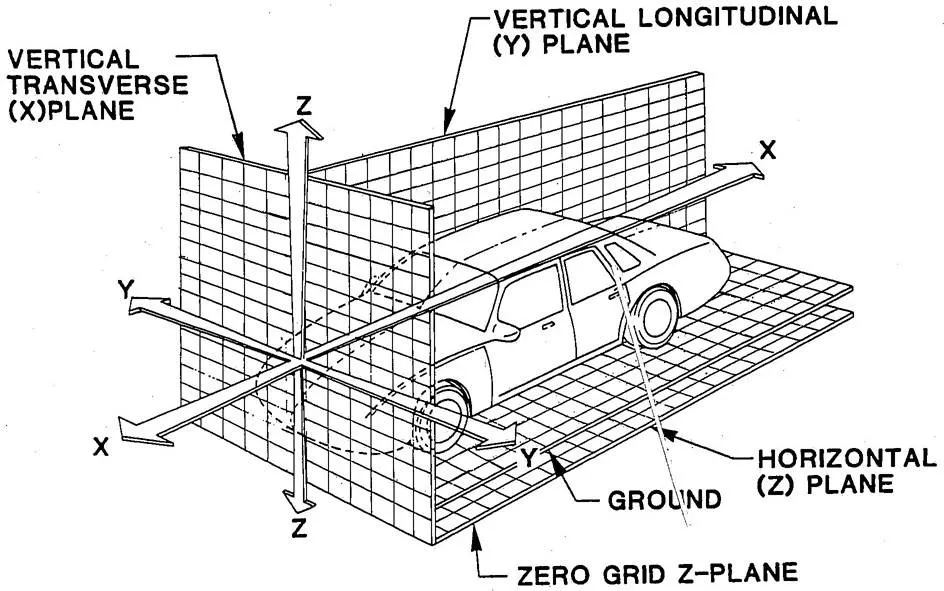
- The measurement from the body planes to the parts are called the body line dimensions.
X = Longitudinal direction[(Fore and After- F/A) or (Front O Line- FOL)]
Y = Transverse direction[(Cross car- C/C) or (Centre O Line- COL)]
Z = Vertical direction[(Up and Down- U/D) or (Bottom O Line- BOL)
Fig shows: Typical body plane of a car
Body line dimensions are essentials for the following reasons:
- It defines exact position of each product in the vehicle with respect to a fixed origin.
- It ensures flawless design for assembly.
- While designing lines, all the designs are carried out relative to the bodylines viz.fixtures,turntables,etc.,
- It assists in easy location of different parts in the vehicle.
- It aims in creating a standardized system.
- It assists in quality check.