Week 4:- Pin Unit Design Challenge
OBJECTIVE:
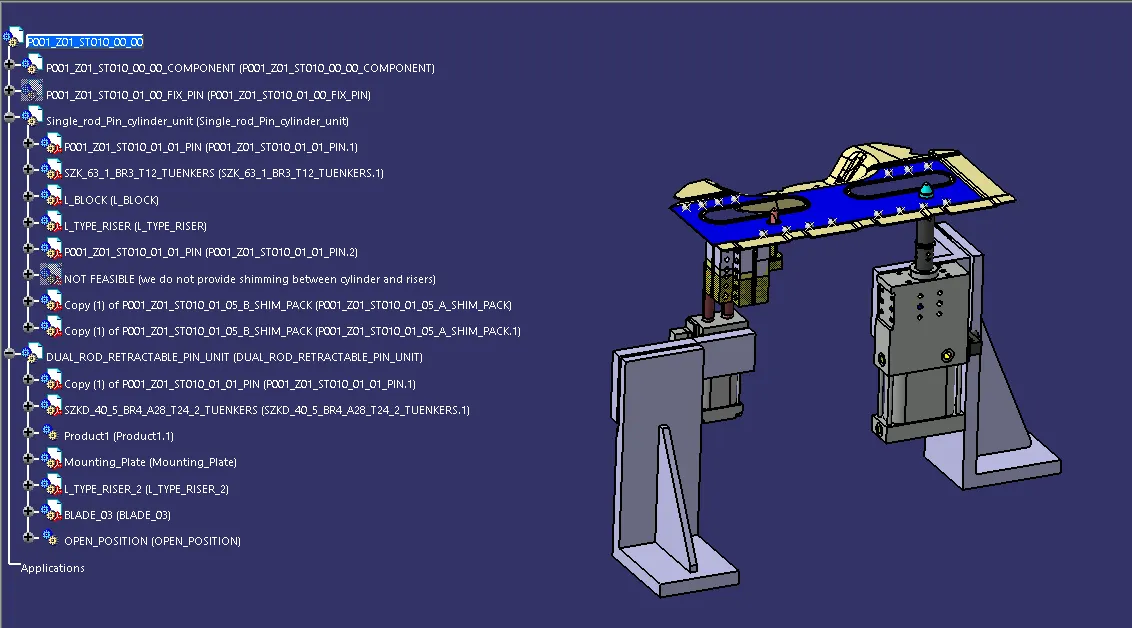
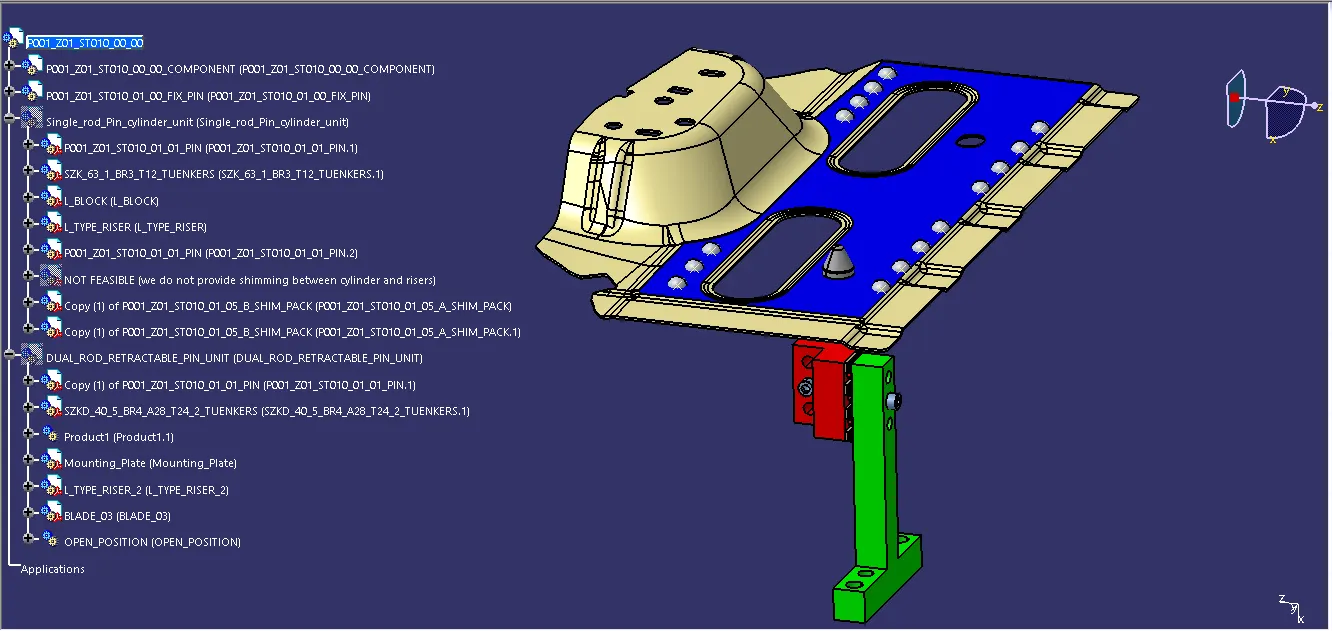
To design 2 different types of fixed pin unit with different pins, riser, blade & block and 2 different types of retractable pin unit with different pins, riser, blade, cylinder & block.
SOFTWARE USED:
CATIA V5
FORMULA & CALCULATION:
Formula to calculate the length of the screw,
Length of the screw = [1.5 X (std. hole size)] + {distance between the surface of the part to the first surface of the other part}
Example:
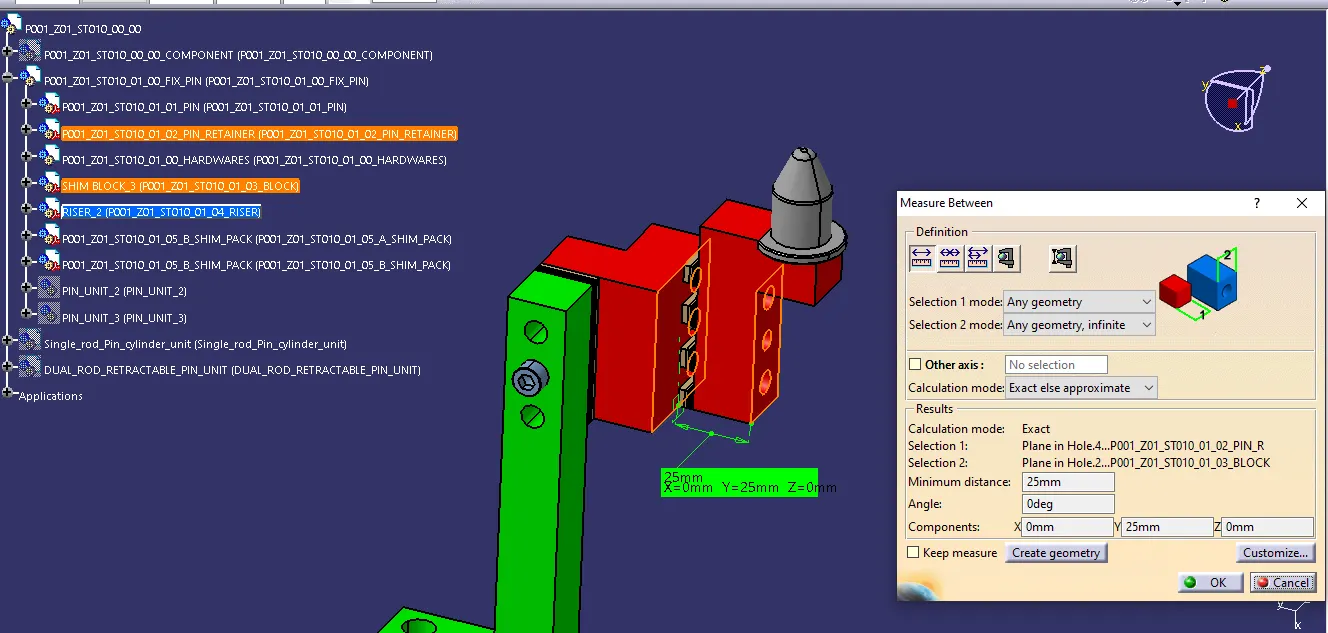
Figure 1. Length calucaltion for length of the screw.
To fix the pin retainer & the shim block using a standard screws we need to find the length of the screw using the above mentioned formula.
The highlighted surfaces shown in the figure are the {distance between the surface of the part to the first surface of the other part}
Since, the given tap holes is M8 & the distance is 25mm as shownin figure then,
Length of the screw = [1.5 X (std. hole size)] + {distance between the surface of the part to the first surface of the other part}
Length of the screw = [1.5 X 8] + 25 = 37 = 40mm Allen cap screw
Then the standard size of the screw should be 40mm for connecting the pin retainer & the shim blocks for this example.
MATERIALS USED:
In general, the materials used for pins, pin retainers, shims, shim block, blades & risers are:
Pin : C45, EN31, SAE 8620 Steel, etc.
Pin retainer : Steel / ASTM A-36, SS type 303 or 304, etc.
Shims/spacer : S.A.E. 1010 CRS FULL HARD, COLD ROLLED STRIP STEEL S.A.E. 1010 FULL HARD, S.A.E. 1020 HRS, etc.
Shim block : STEEL ASTM A-36, NM Stainless, STEEL ASTM A-36, SS type 303 or 304, etc.
Blade : STEEL ASTM A-36, etc.
Riser : STEEL ASTM A-36, etc.
HARDNESS:
In general, the hardness of the materials for pins, pin retainers, shims, shim block, blades & risers are:
55 - 60 HRC / 58 - 62 HRC to a depth of 0.5 - 0.7 mm after grinding.
SURFACE FINISH:
In general, the hardness of the materials for pins, pin retainers, shims, shim block, blades & risers are:
Pin : Chrome plating, Zinc coating, Pins with TiN codes shall have 1 to 2 microns of nitride added to surfaces.
Pin retainer : BLACK OXIDE FINISH, No black oxide finish for "SS TYPE" components (SURFACES TO BE FLAT, PARALLEL &
PERPENDICULAR TO O WITHIN 0.015 T.I.R).
Shims/spacer : BLACK OXIDE FINISH (SURFACES TO BE FLAT AND PARALLEL TO
WITHIN 0.015 mm T.I.R).
Riser : SURFACES TO BE FLAT, PARALLEL & PERPENDICULAR TO WITHIN 0.015 T.I.R.
PIN TOLERANCE:
The pin tolerance fora geo pin will be of closer tolerance i.e -0.15mm & for respot pin is of -0.28mm.
PURPOSE OF PIN UNIT:
As by 3-2-1 locating principle, the introduction of two pins helps to arrest the 6 degrees of freedom (4 axial & 2 radial movements) whereas other 6 degrees of freedom are arrested by introducing minimum three supports.
Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
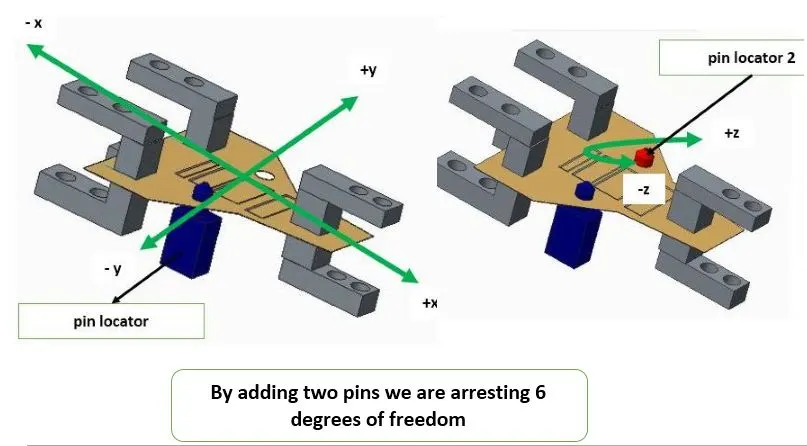
Figure 2. 3-2-1 Principle concept (Arresting 6 DOF by introducing 2 pins)
FUNDAMENTALS OF PIN UNIT DESIGN:
It is necessary to have two pins to locate a car panel. And here one pin must arrest 4 way (i.e. 4 translation) & other must have arrest 2 way (i.e. 2 rotational) of a car panel.
Pin should engage 3 to 5mm from car part entry surface.
All pin should be accommodated with 2 way adjustable shims irrespective of direction of arresting.
Round pin should be used in case of 4 way arresting of car panel if the hole is round.
Round pin can be used for 2 way arresting of car panel only if the hole is slot.
Diamond pin should be used in case of 2 way arresting of car panel if the hole is round.
Diamond pin should be used in case of 4 way arresting of car part if the hole is slotted.
The axis of the car panel hole & the axis of the pin should be same in general.
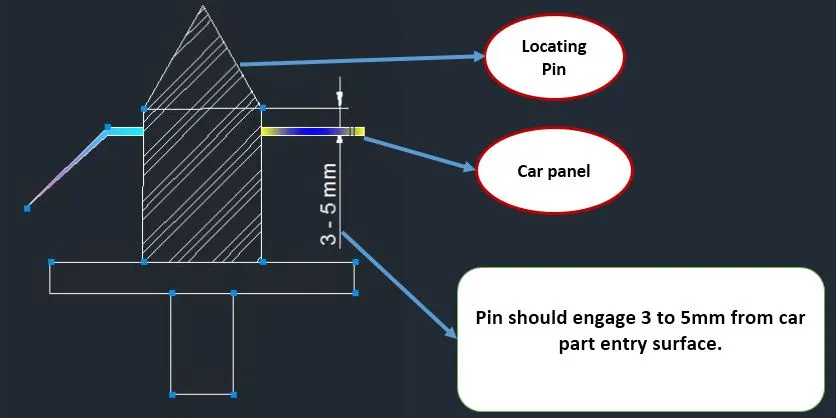
Figure 3. Shows the 1st point in the fundamentals of pin unit design.
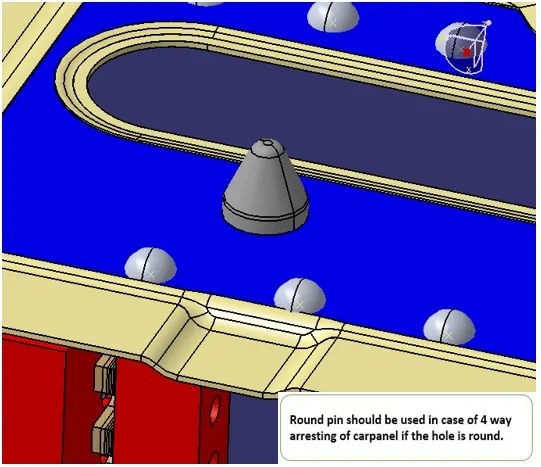
Figure 4. Shows the 3rd point in the fundamentals of pin unit design.
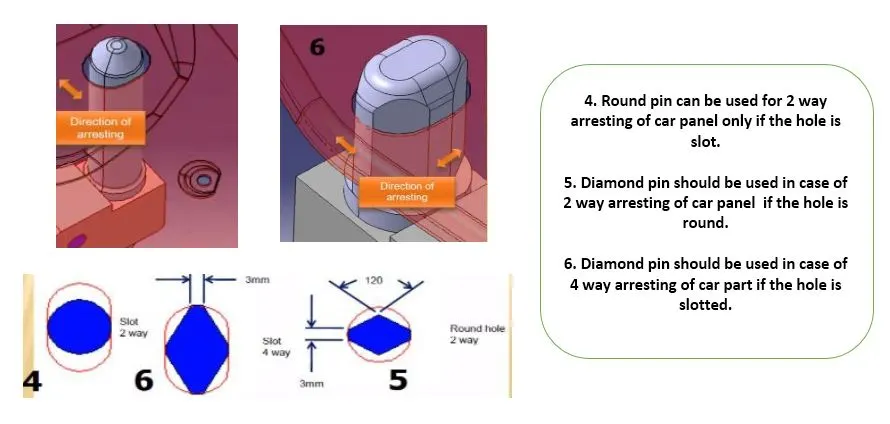
Figure 5. Shows the 4th, 5th & 6th point in the fundamentals of pin unit design.
TYPICAL PARTS OF PIN UNIT: The different parts of the fixed pin units are as follows,
Pin.
Pin retainer.
Shims.
L-block/shim block.
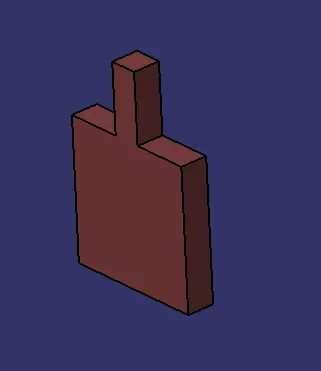
Blade.
Riser.
a. Pin:
It is used for the location purpose of the panel.
Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
There are dozens of styles of locating pins that can be utilized in a design.
A pin can either be a make part or a standard part also. Below I have shown the commonly used pins. One of the most common pins is a stepped pin with either small or large head.
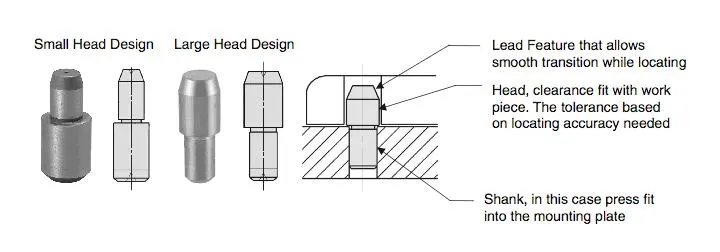
Figure 6. Types of locating pin.
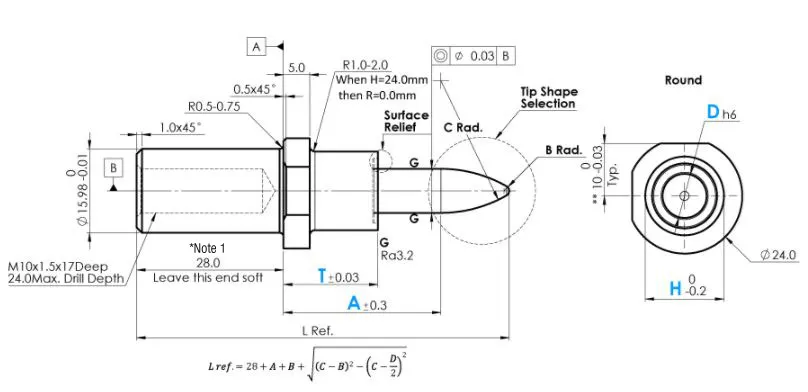
Figure 7. NAAMS standard locating pin (6 way small head) - Make: MISUMI
Consideration while designing & manufacturing of pins:
Pin should have grinding surface on shaft with fits on to which the pin retainers will be fitted.
The mounting surface of the pin should be a fine machined surface.
A pin should have a step machine surface to lock the rotation, which matches with the pin retainer.
The mounting surface of the pin retainer to the blocks should be machined surface.
All machined planes should be perpendicular to the axis of pin shat.
Pin must have a fastening provision like tapped hole from the bottom or a v- grove from the side.
A pin must be hardend ( 55 - 60 HRC) & black oxide finish in general.
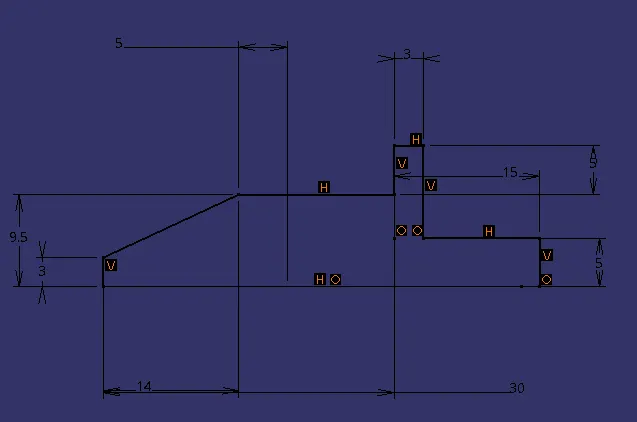
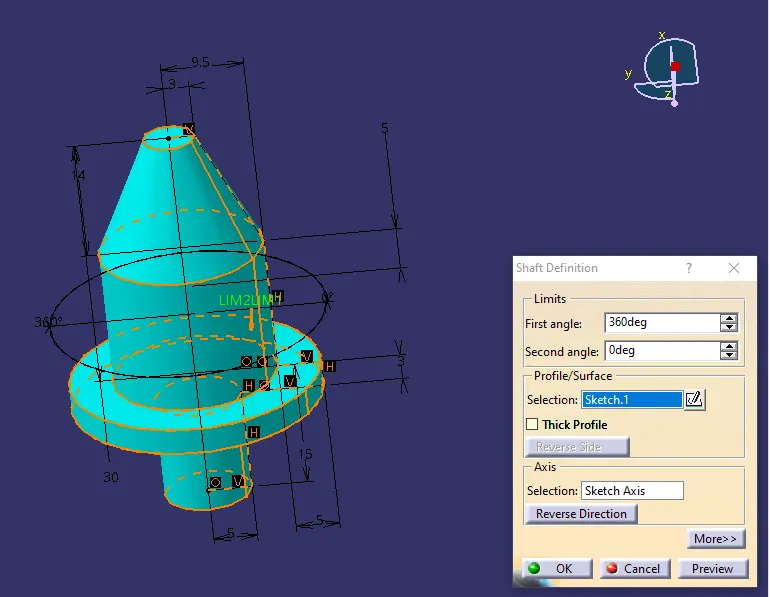
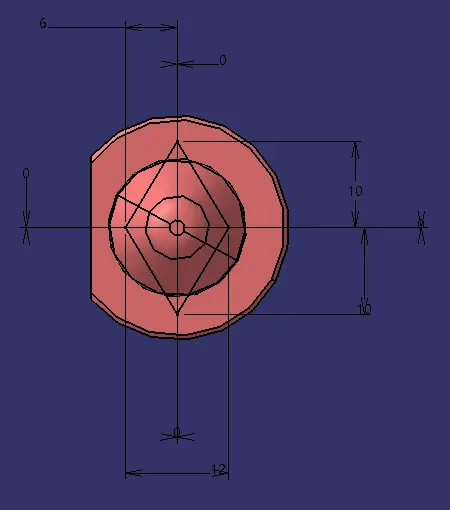
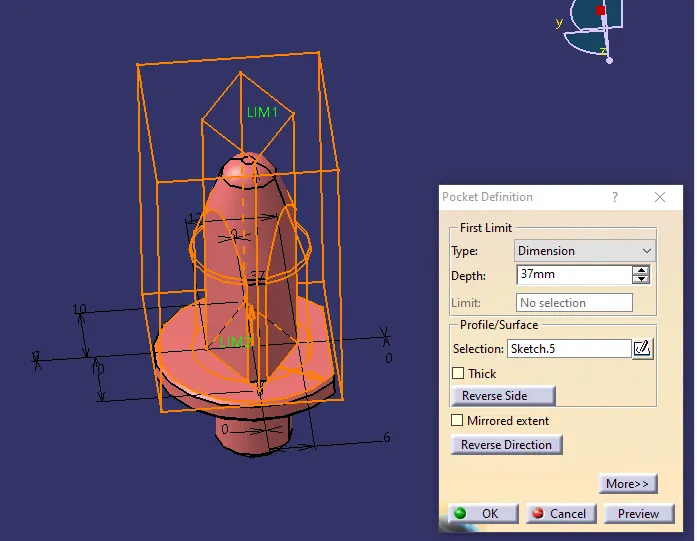
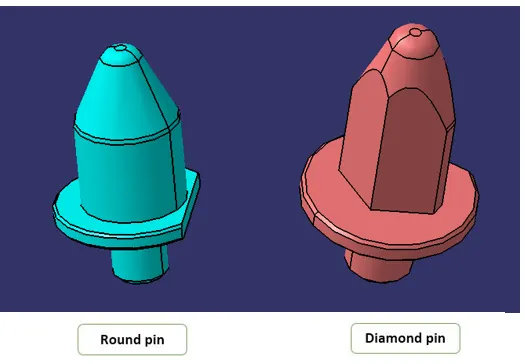
Figure 8. Locating pin.
The above shown picture are the CAD model of different types of pins used in the projects.
b. Pin retainer:
A pin retainer is a part which holds the pin in position, the pin retainer can either be a make part or a standard part also.
Pin retainer is used to hold the locating pins firmly.
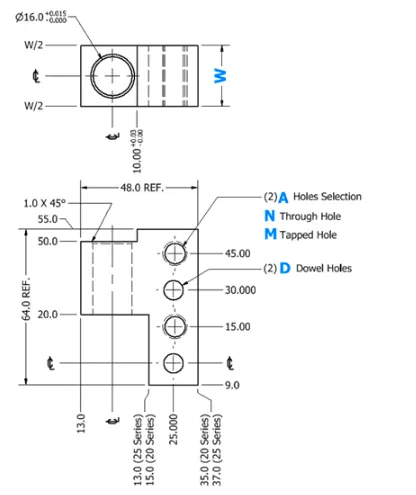
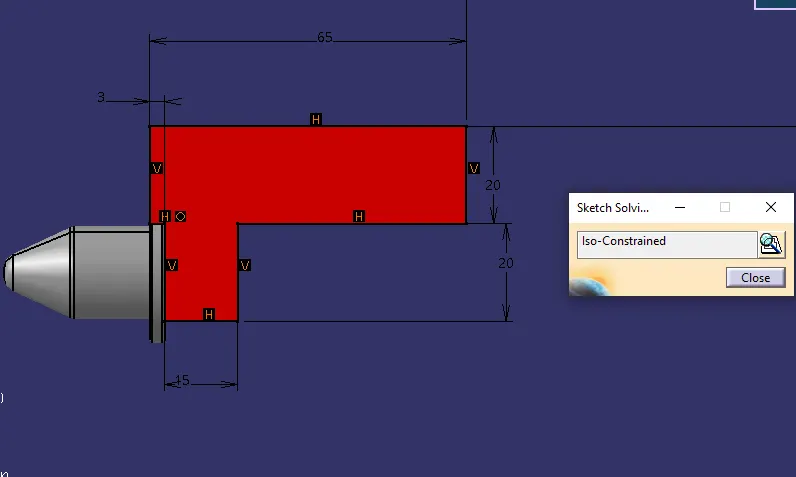
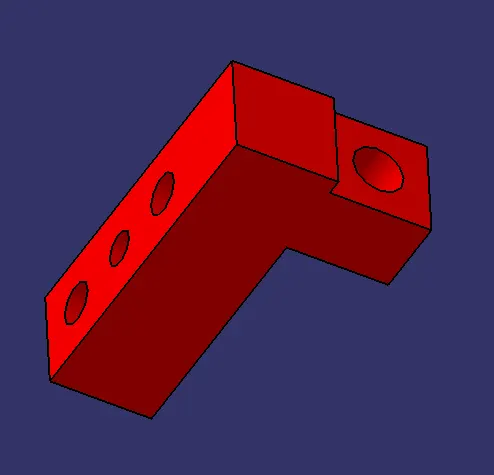
Figure 9. NAAMS Standard - Pin Retainer (APR L shaped 4-side holes)
Consideration while designing & manufacturing of pin retainers:
Pin retainer should have a hole with a fit, on to which the pin will be fixed.
The pin mounting surface of the pin retainer should be a fine machined surface.
The pin mounting surface of the pin retainer should have the step to lock the rotation of the pin.
The pin mounting surface of the pin retainer to the blocks should be a machined surface.
The pin retainer will be fixed to a block or a L - block to the riser with 2 dowel holes & at least with one screw hole to maintain the tolerance.
c. Shims:
Shim is generally used to adjust the design to manufacturing deviation(To avoid stack up tolerances).
In general, A shim is a thin and often tapered or wedged piece of material, used to fill small gaps or spaces between objects.
Shims are typically used in order to support, adjust for better fit, or provide a level surface.
Shims may also be used as spacers to fill gaps between parts subject to wear.
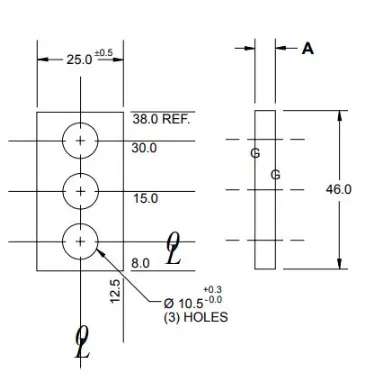
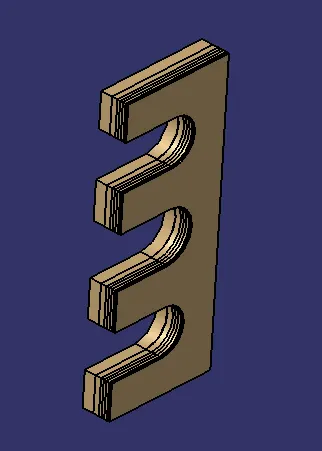
Shims are the small parts which comes with the thickness of 0.1mm,0.2mm,0.5mm,1.0mm etc.
These will compensate the stack up tolerance which reflects at the Mylar's.
We give tolerance to all parts of the fixture. Due to this tolerance the Mylar's will either lift up moves down from its defined position.
To adjust the Mylar's for getting the defined position we use shims.
Shims will be added above the Mylar for adjusting according to tolerance.
Application of shims:
In automobiles, shims are commonly used to adjust the clearance or space between two parts. For example, shims are inserted into or under bucket tappets to control valve clearances. Clearance is adjusted by changing the thickness of the shim.
In assembly and weld fixtures precision metal shims are used between two parts so that the final production parts are created within the product drawing's specified tolerance.
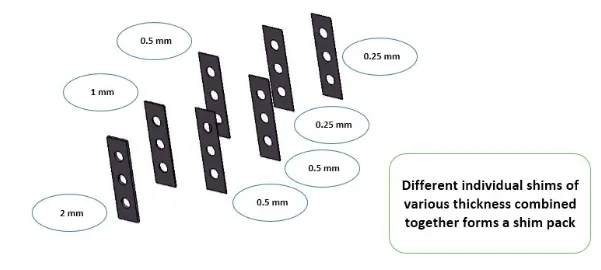
Figure 10. Exploded view of Shim pack (The above shown thickness of shims are used to form shim pack in this project).
d. L - Block / shim block:
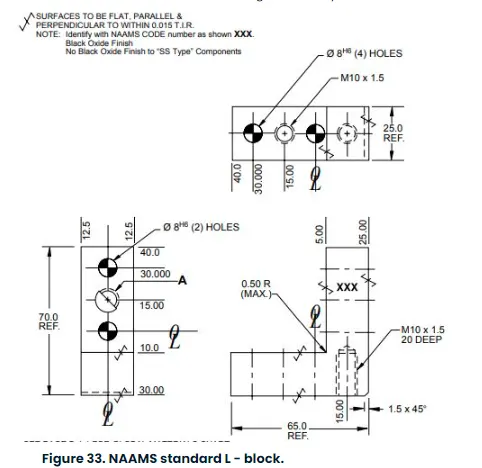
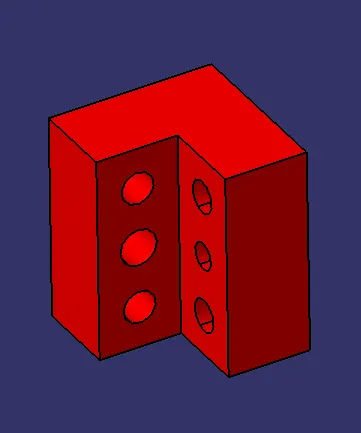
These parts are mainly used to accommodate the shimming directions as per fundamental in general.
Also in some cases used for other design feasibility.
e. Riser:
Riser is a manufacturing part used to raise/height the assemblies of fixtures.
One end of the raiser will be attached to the base unit while the other end will be attached to the Blade.
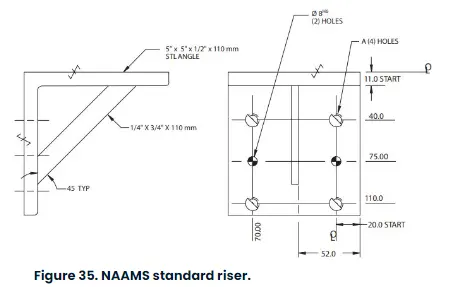
It is a part on which all the parts of a unit are mounted on the base plate of a tool. In general, the riser can either be make part or a standard part.
Raiser can be of two types. They are,
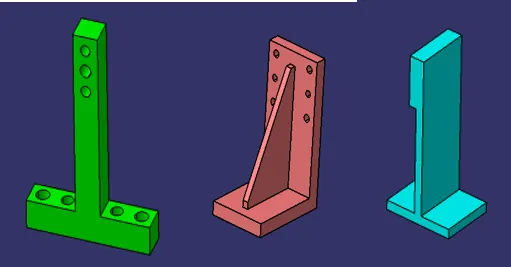
'L' type risers.
Square tube risers.
'L' TYPE RISERS: 'L' type risers are of welded type. Where the stiffener will be added at the centre for support. As shown in the below figure the wedge shaped structure is known as stiffener which is used as a support / to withstand load.
Square Tube Risers: Square tube raisers are of frame type.
f. Blade:
Dowel holes & machined surfaces in pin unit:
All make parts which are to be assembled with tolerance should be designed with 2 dowel holes & at least of 1 to 6 threaded or free hole (depends on size). And to be fine machined for the mounting surface with 3 to 5mm step machining (SURFACES TO BE FLAT, PARALLEL &
PERPENDICULAR TO O WITHIN 0.015 T.I.R).
BOUGHT OUTS:
Bought outs used in this projects to design a pin unit are,
Cylinders.
Fasteners.
1. Cylinders: Pneumatic cylinder (Make : Tunkers)
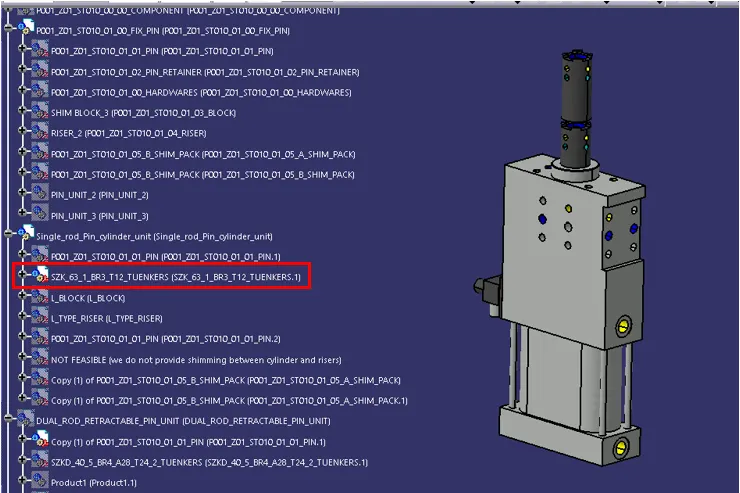
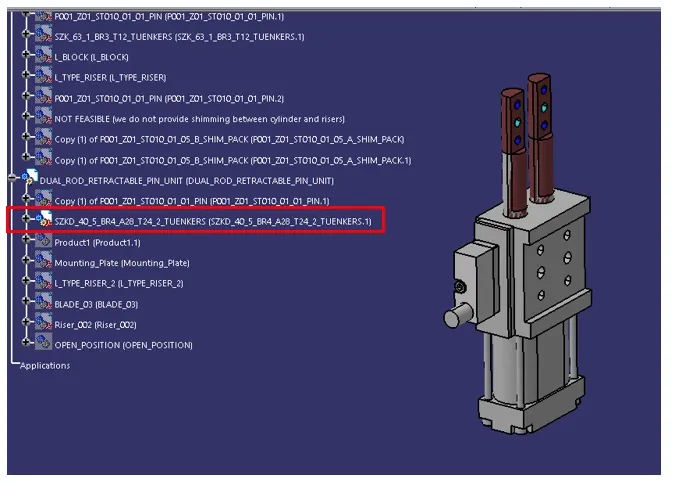
Retract cylinder with side mounting on piston rod for offset centre pins, Flat housing of high-strength aluminium material, Drive via oval-shaped oblong cylinder Ø 40/63 for thrust and tensile forces of up to approx. 1200 N, Push rod secured against twisting double-supported in bronze bushings, Integrated inductive sensors, Guide rod secured against twisting, 40 mm combined stroke 40 mm, intermediate stroke lengths upon request.
2. Fasteners:
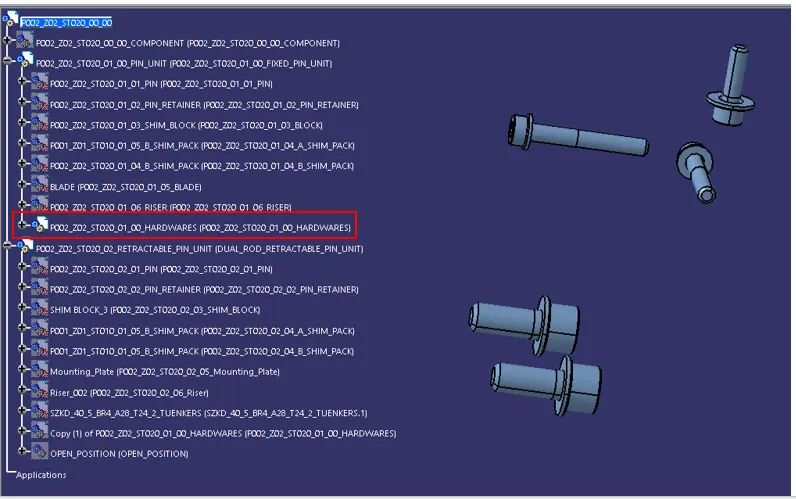
Hexagon allen cap screw (std: EN_ISO_4762_Steel hexagon cap screw).
Washer (Std: EN_28738_8_STEEL GRADE_CLEVIS_PINS_PLAIN_WASHER).
TYPES OF PIN UNITS:
The types of pin units are: Fixed pin unit & Retractable pin unit.
FIXED PIN UNIT:
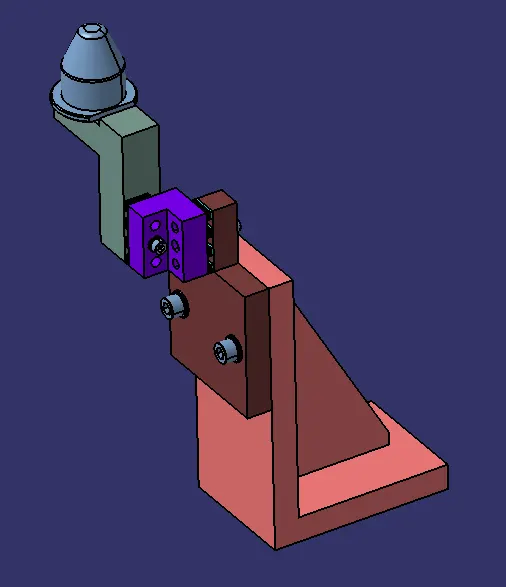
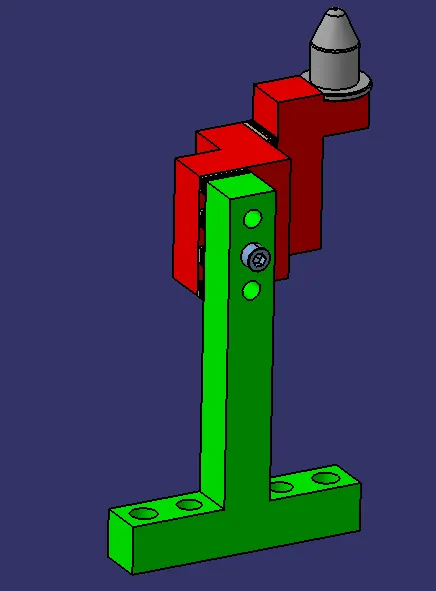
Fixed pin unit is a unit designed to locate the car panel using pins.
Pin, pin retainer, shims, blocks, blade, riser are the part of fixed pin units in general .
pin retainer is used to hold the pin firmly.
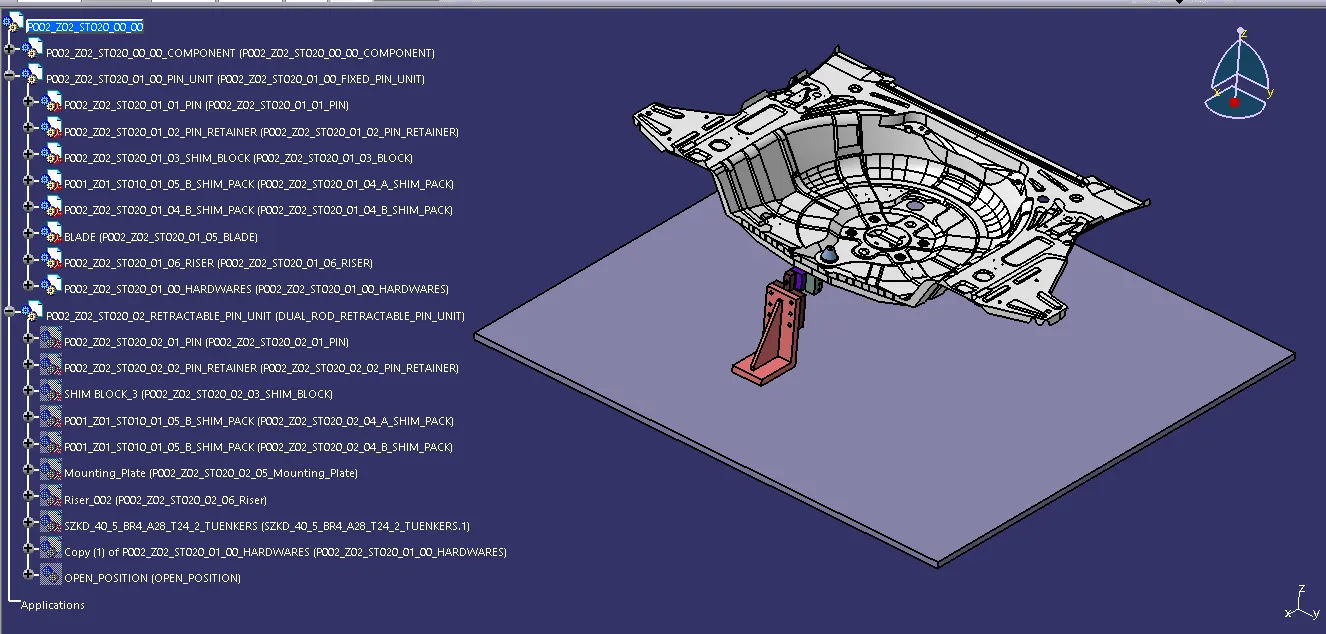
Figure 7. Shows the Principle Locating Point (PLP) in fixed pin unit.
Principle locating points is a hole in which we locate the panels. PLP holes must be very much precise.
RETRACTABLE PIN UNIT:
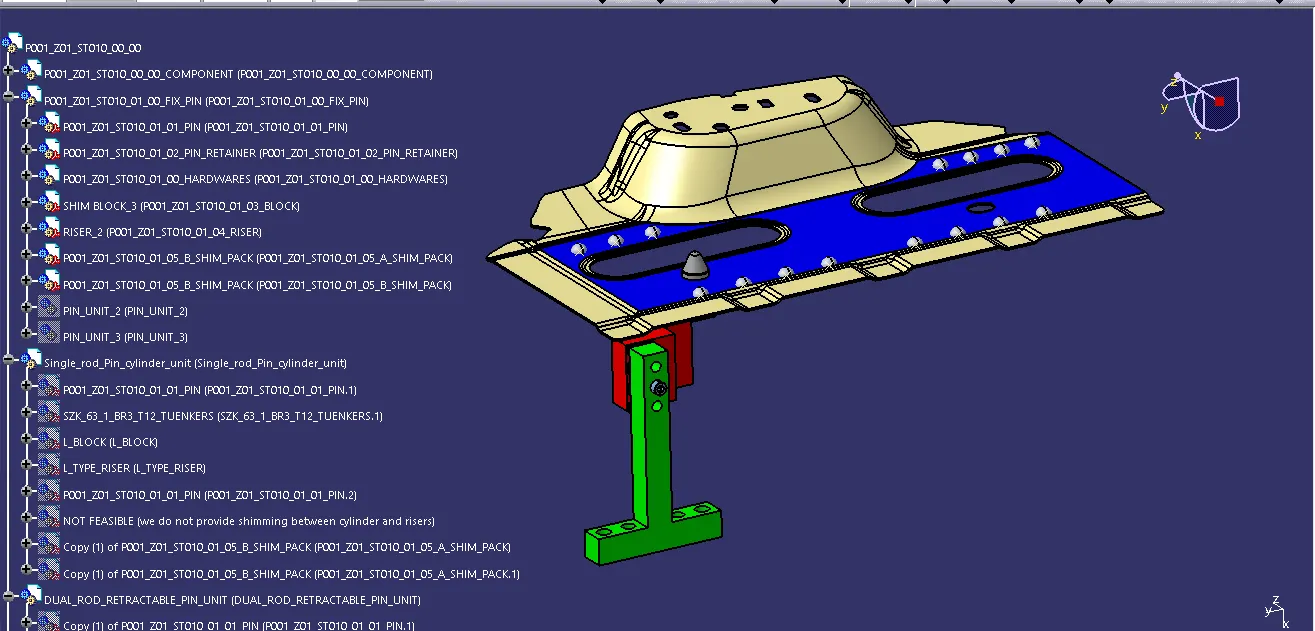
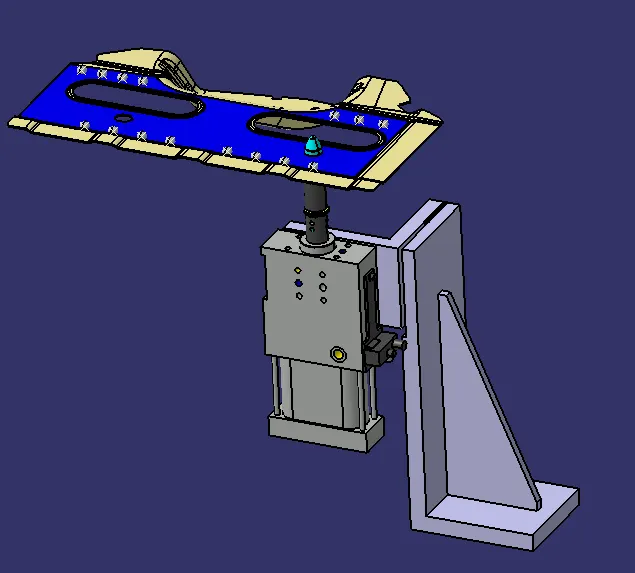
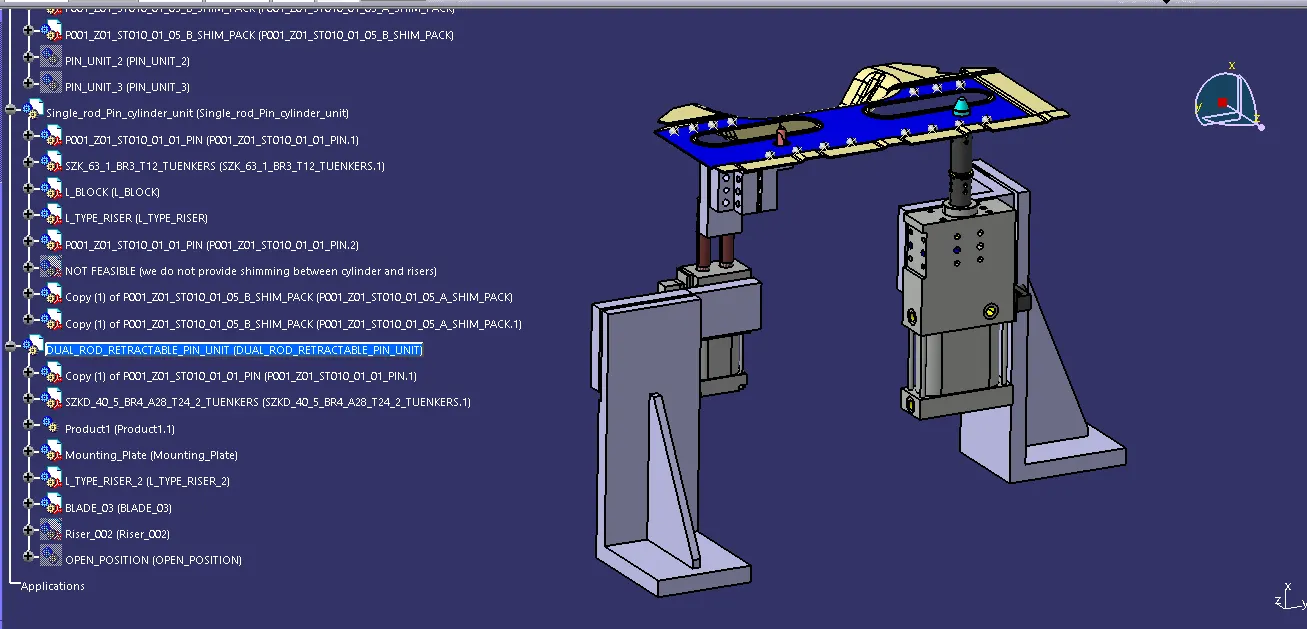
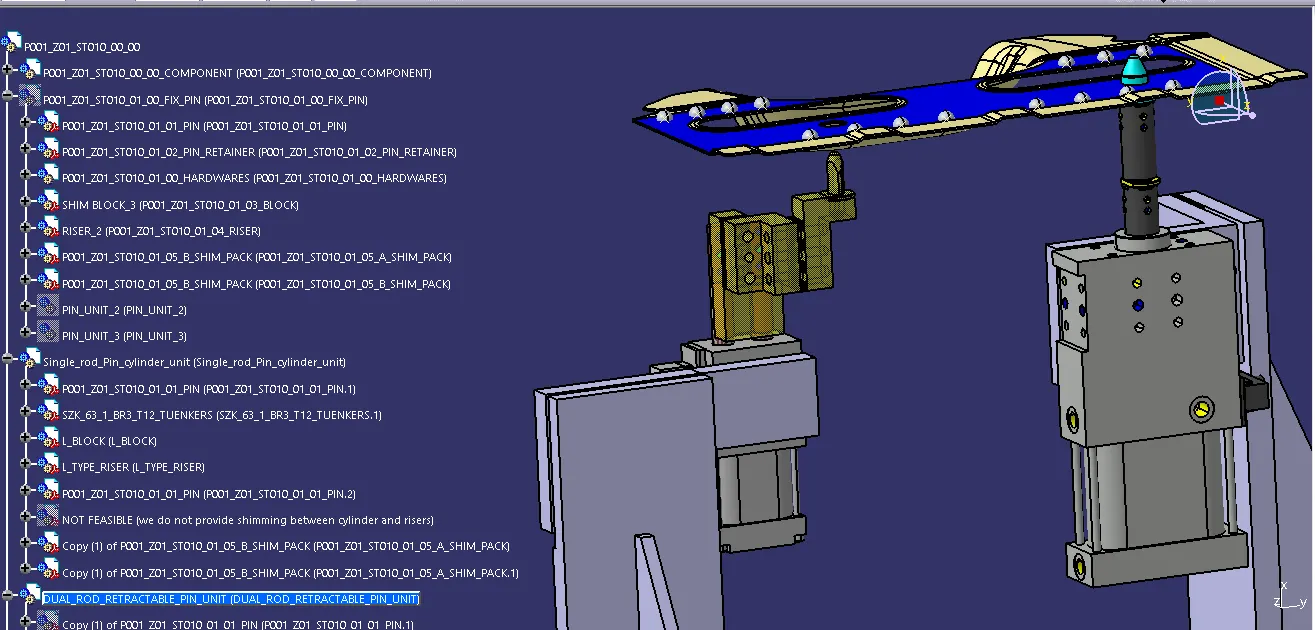
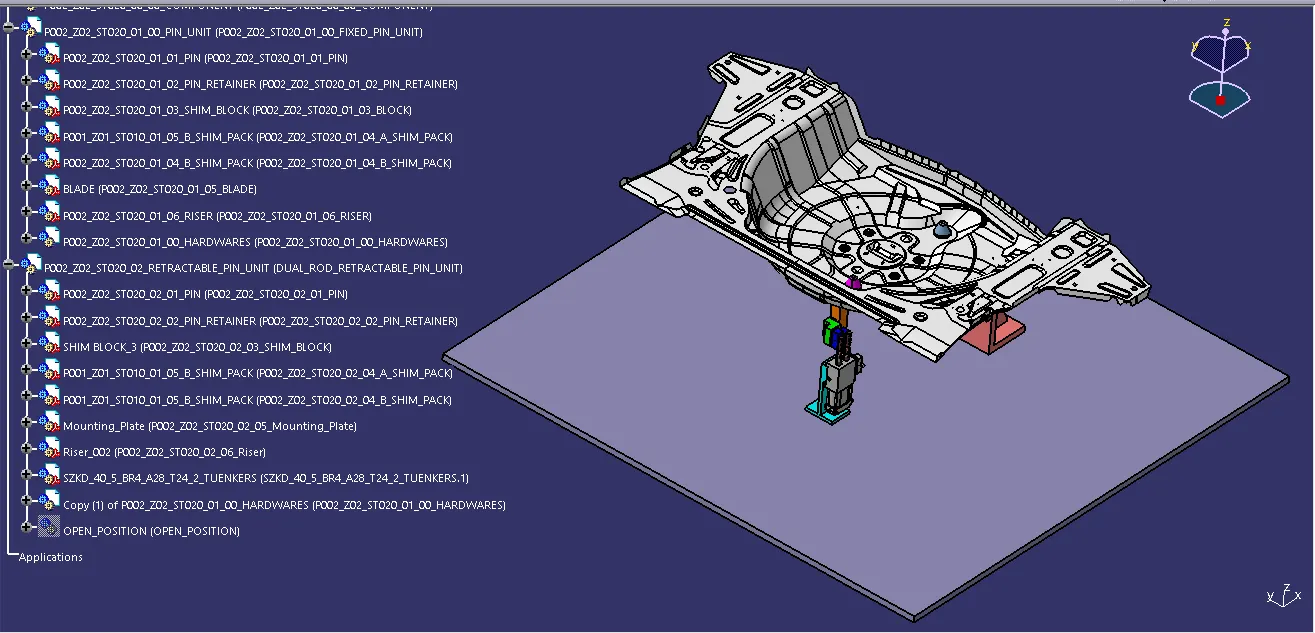
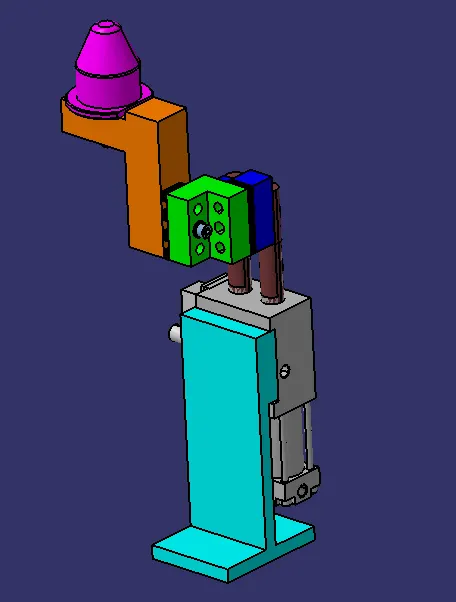
A retractable pin unit is a unit designed to locate the car panel using pins, but the entire pin package parts will be mounted on the retractable pneumatic cylinder.
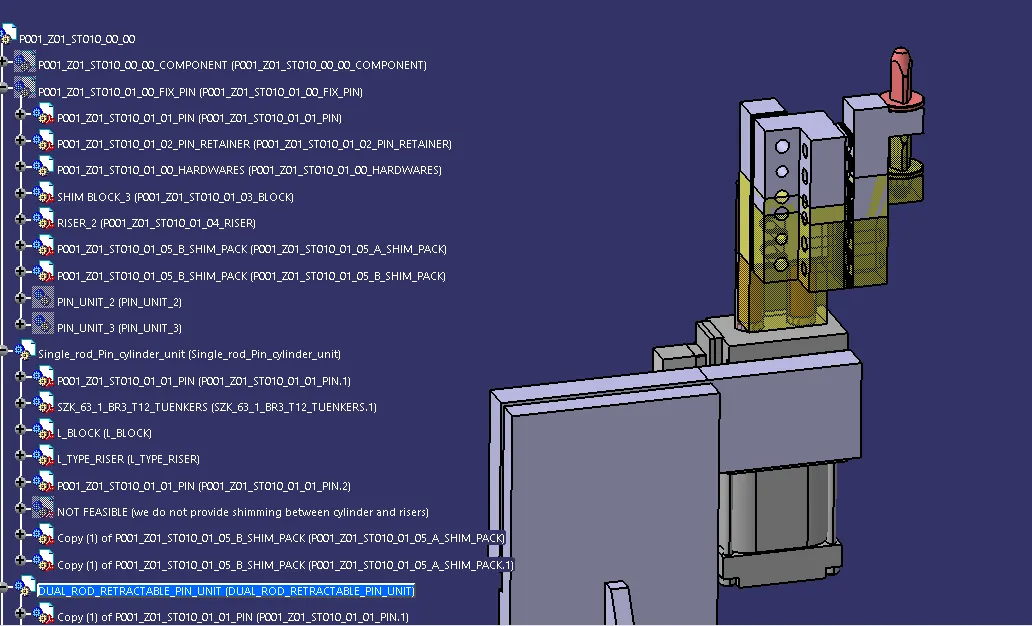
Pin, shims, L Block, pneumatic retractable cylinder, riser are the parts of retractable pin unit.
CLOSED POSITION
OPEN POSITION
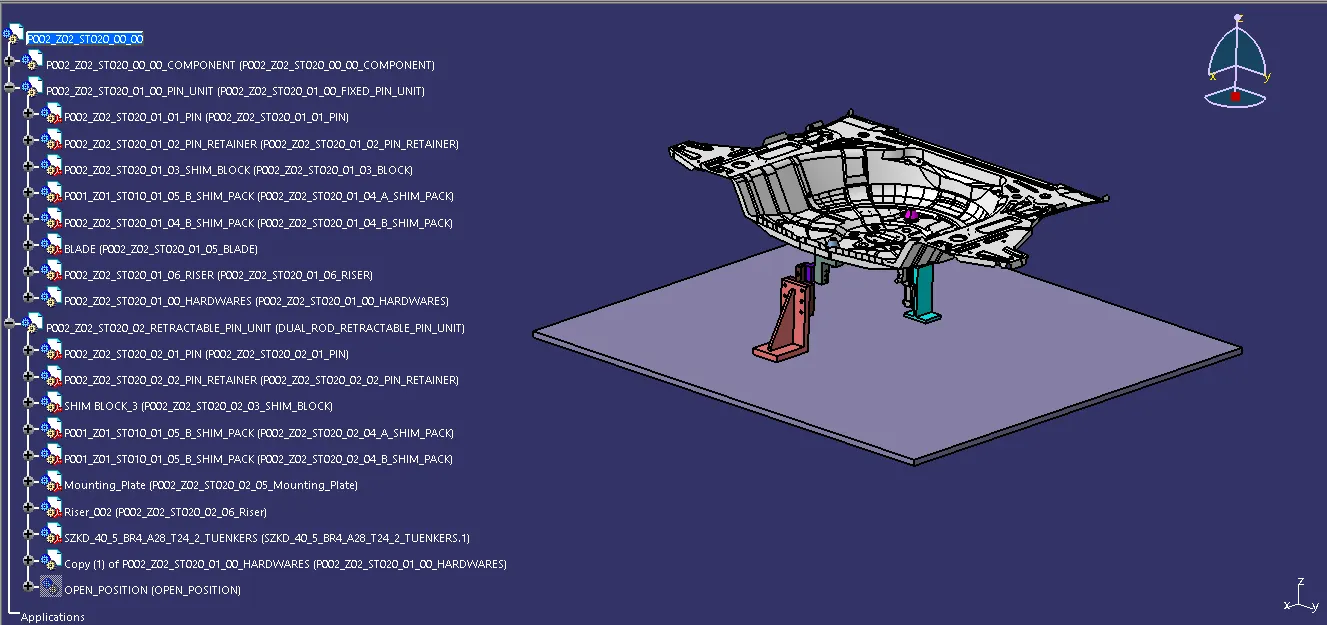
FINAL ASSEMBLY: