Week 3:- BiW Fixture Design Methodologies Challenges
- What is Design Methodology?
The design methodology is nothing but the steps followed during the concept designing stages of fixture design. The various stages of design methodologies are
- Purchase order
- Inputs from customer
- Percentage of completion criteria
- Design outputs
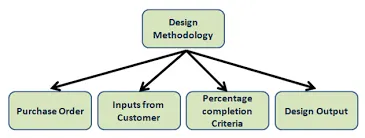
Figure_ various stages of Design Methodologies
- Purchase Order
- A purchase order is a commercial document and the first official offer issued by a buyer to a seller indicating types, quantities, and agreed prices of product or services.it is used to control the purchasing of products or services.it is used to control the purchasing of products and services from external suppliers, purchase orders can be an essential part of enterprise resource planning system order.
- A purchase order is an order from a customer for the start of the work
- After the offer has been finalized customer will release the LOI/PO (purchase order)
- Once PO is released, we have to start the work
- After PO from the customer, we have to prepare the schedule.
- A purchase order is the confirmation document from the customer to proceed with the committed work for them
- Inputs From Customer
The inputs from the customer are as below
- Functional Requirements: the purpose or the function of the fic=xture will be given as inputs from the customers like what are the process the fixture is going to do I.e. welding, Gluing, reverting, or whether it is checked fixture acts.
- Preferred standards: As we know different companies follow different standards. we will be following the customers. By following standards the time of the projects. as for the standard parts, they can be easily replaced from the used fixture to the new fixture which reduces the cost.
- Car products: The inputs we get from car products are GD&T, parts list, Cad files of the car parts, Clamp plan product assembly process sheet
- Layout: layout shows the entire assembly plan to understand the process. The layout provides the information of flow of parts, station pitch. robot station, Accessories like tool changers &tips dressed, sub-assembly links, platform height, loading/unloading sequence/height
- Ergo Data: As same as preferred standards, different companies follow different standards of Ergo data. We have to follow the customer standards of Ergo data. The inputs of Ergo data will be given by the customer mostly in case of manually operated fixtures/manual fixtures. The Ergo data is mainly used to make the operator comfortable which may lead to improved efficiency in cycle time & production. Ergo data provide inputs like Platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/ assemblies are visible while clamping or loading & unloading. Also provides information like Loading height, working safety zone of the operator, etc.
- Weld study: Weld study is the important input given by the customer.it gives details about the study of particular guns that we use for welding. also, the dates like no. of the weld. position of weld in the component will be given in short, weld study includes weld gun detailing weld matrix & weld point.
- Standard detailing Templates: the inputs include the detailing templates of 2d cad drawing as per the customer standards .so we have to follow the detailing template as per the customer standards.
- Percentage of completion criteria:
- it is followed in the designing stages & dispatch of welding fixture
- it helps to track or identify how many tasks are completed &how much to go further for completing a fixture
- input & concept design 0-25%
- concept approval &simulation check 25%-40%
- design freezing &detailing 40%- 85%
- check & final dispatch 85%-100%
- the above-mentioned percentage is the percentage of stage-wise completion criteria of the projects
- Design output:
- The output is 3d model & 2D drawing of the tools
- Which includes key sheet & layout sheet for unitized tool whereas no need of key sheets for non unitized tools
Hence, the design methodologies are explained in detail.
2. What are the inputs required from the customer to start designing a Fixture?
The inputs required from the customer to start designing a fixture are as follows
- Functional requirements
- Preferred standard components
- Car products
- Layouts
- Ergo-data
- Weld study
- Standard detailing templates
- Functional requirements:
- The purpose or the function of the fixture will be given as inputs from the customers like what are the process the fixture is going to do i.e welding (spot or seam weld ) gluing, riveting, hemming, or whether it is checking fixture or storage racks, etc.
- It is one of the basic requirements to get from the customer to start designing a fixture.
2. Preferred standard components:
- As we know different companies follow different standards we will follow the standards followed by the customers
- By following standards the time of designing and manufacturing of parts will be saved which will be automatically minimizing the time time of the projects.
- As for the standard parts.it can be easily replaced from the used fixture to the new fixture. which reduce the cost
- Some of the preferred standard components used in BIW fixtures are given below
- Standards like ABB, NAAMS, DESTACO, ZYTRAN, TUNKERS are used in the design & manufacturing of fixtures.
- Standard Parts like Risers, L-blocks, Retainers, pins, NC blocks, shims, etc.
- Components like clamps, cylinders, slides, switches, sensors, etc.
- Weld guns, Tip dressers, Tool changers, etc. Tip dressers are to sharpen the tip of the tools whereas Tool changers are used in robots to do the various processes. As robots are too costly, tool changers are used.
Below I have explained some of the standards in detail
ABB- It is a Robots manufacturing company. some examples of description of standard robots are Robust IRB 7600 robots, which can hold the panels securely and accurately in place while IRB 6640 robots perform the welding.
The below picture shows the welding line installed at Great Wall Motors (GWM) recently opened an internationally acclaimed automotive plant in Tianjin, China. One of the factory's most highly publicized and productive manufacturing lines is the ABB welding line, which comprises among other things a fleet of ABB robots and patented ABB framing and hemming technologies.
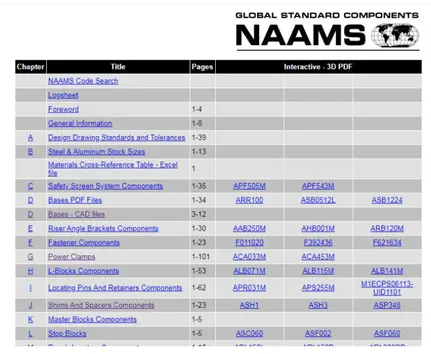
Fig NAAMS catalog
We can also import some of the cad files in 3D/2D from the online NAAMS catalog. the below picture shows the Dwg. the file of standard Base ABS1212-1200 X 1200. which I found from the online catalog
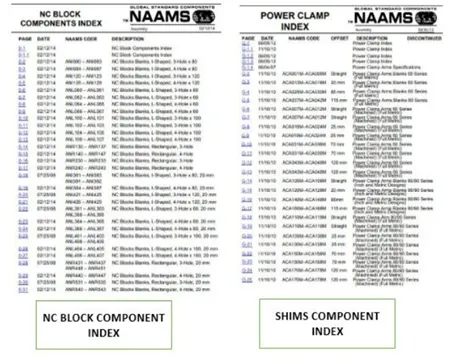
Fig NC block index& shims index
We can get the NAAMS standard codes from the required parts index
The catalog will contain drawings with standard dimensions. As per our requirements, we should choose the standard part/components by referring to the standard dimensions mentioned in the catalog. Also, the standard will be useful for assembling the components easily without any offsets.
The below picture shows the standard dimensions for the power clamp arm (60 series)
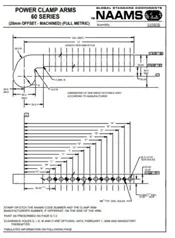
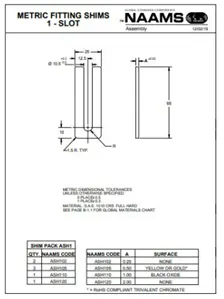
Fig-power clamp arm60 series Fig- NAAMS standards of metric fitting shims (1-slot)
DESTARCO:- It is a Dover Corporation company.DESTACO is a manufacturer of work holding devices like manual clamps, pneumatic clamps, grippers, conveyors, automatic tool changers, end effectors tolling, etc
The below pic shows some of the products of DESTACO
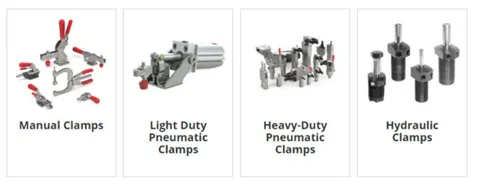
Fig Manual clamping, pneumatic & power claiming system of DESTACO
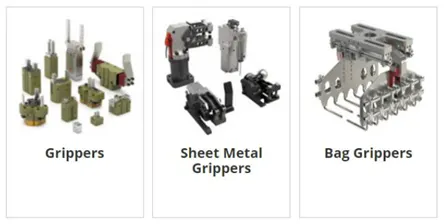
Fig Grippers of DESTACO
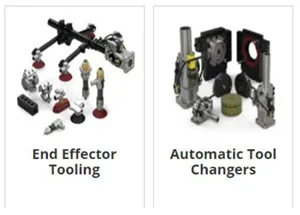
FIG Robot tooling DESTACO
ZYTRAN – Zytran automation is a gripper manufacturing. Grippers by Zaytran are universally applicable “out-of-the-box”. the use of the third-generation ZYATRAN technology and the selection of super tough, corrosive resistance material allow these products to efficiently serve day-to-day as well as tough, nearly impossible along stroke gripper applications but are priced competitively with commodity product ZAYTRAN gripper technology provides precision in extreme environment such as clean rooms grinder loading. active and die casting
ZAYTRANS presented helix synchronization system facilitates extremely long strokes in additional wear is minimized because the force and synchronization systems are independent
As per the size and specifications, some of the ZYTRAN product grippers are,
- Grippers for “normal” size jobs and clean rooms -MAGNUM GRIPPERS
- The GPL and GPAL mid to large gripper lake our classic design and make them lighter with more force -GPAL Gripper.
- For a really big gripper job,500pounds (2200N) of force per jaw, strokes to 350mm-X-RAY – S LOND STRIKE GRIPPER
Some of the applications of ZYTRAN Gripper are small below including pic they are
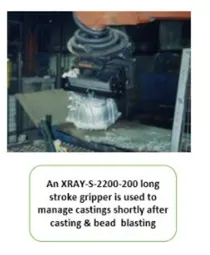
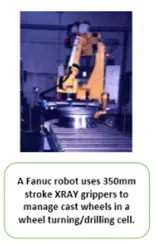
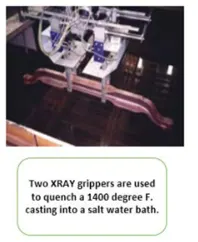
Fig some of the applications of ZYTRAN grippers
TUBKERS – Truckers are the manufacturing of automation products grippers robotic welding &Clamping technology. Clamp manufacturing by TUNKERS stand out due to universal applicability and distinguishing construction features the extensive product range comprises pneumatic, hydraulic, electric, and manual clamping systems
Some of the products of TRUCKERS are shown in the below picture
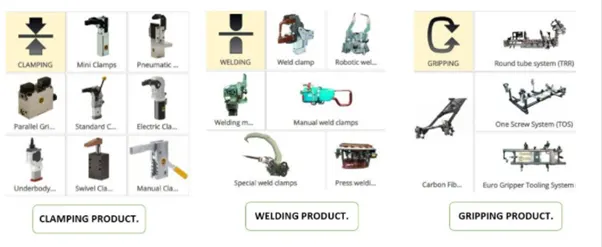
Fig some of the products of TUNKERS
3. CAR PRODUCTS: the inputs we get from car products are GD&T, part list, cad files of car parts, clamp plan, product assembly process sheet
- GD&T: it provides information on locating pins, rest, clamp, damp& slide unit information of each station. Also include the information of the sequence of openings of clamp Damps & slide stroke information
- PART LIST: it gives the lists of parts which are going to assemble in the fixture the list contains the information o part number, part name, revision of fixture, part thickness, etc
- Clamp Plan: clamp plan provides the information of the location of the pin, rest units clamp unit, dumps, etc, it is the important input from the customer. the clamp plan /position should not be changed without the knowledge of the customer
- 3D CAD FILE: the 3D model of the car part will be given from the customer from the 3D model we will be developing our fixture design process. The 3D cad files will be in the format of step file (step) or IGES file(igs.)
- PRODUCT ASSEMBLY PROCESS SHEET: It gives the information of stage-wise assembly process like how the parts move from one assembly station to another after the completion of the joining process
4. LAYOUT:
- The layout shows the entire assembly plan to understand the process
- The layout provides the information of flow of parts, station pitch, robot station, Accessories like tool changers & tip dressers, sub-assembly links, platform heights, loading /unloading sequence/ height
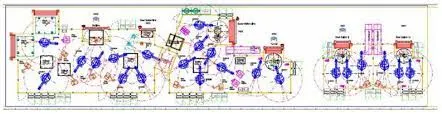
Fig Layout
5. ERGO DATA:
- As some as preferred standards, different companies follows different standards of Ergo Data
- We have to follow the customer standards of ergo data
- The input of ergo at will is given by the customer mostly in the case of manual operations fixtures/manual fixtures.
- The ergo data is mainly used to make the operator comfortable which may lead to improving the efficiency in cycle time & production
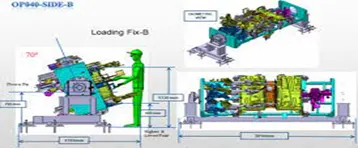
Fig Ergo data
- Ergo data provide inputs like platform height, maximum & minimum reach from operations to fixture, maximum 7 minimum heights of the fixture, whether the child parts/assembly are visible while clamping or loading & unloading
- Also provides information like loading heights works safety zone of operations etc.
6. WELD STUDY:
- Weld study is the important inputs given by the customer it gives details about the study of particular gun that we use for welding
- Also, the data like no. of weld position of weld in the components will be given
- In short, weld study includes weld gun details, weld matrix & weld points
- Generally, weld point will be given in spheres
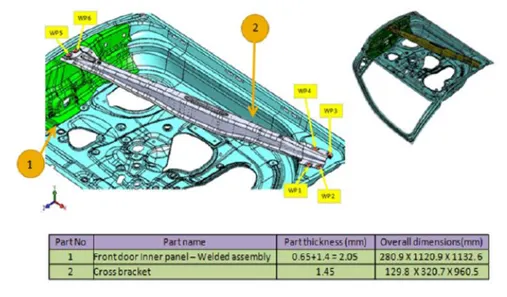
Fig weld study (as it shows t is Geo weld points)
6. STANDARD DETAILING TEMPLATE:
- This input includes the detailing templates of 2D CAD Drawing as per the customer standards
- So we have to follow the detailing templates as per the customer standards
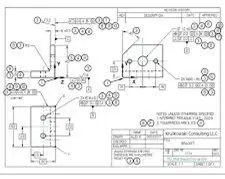
Fig standard detailing template
Hence, the inputs required from the customer to start designing a fixture are explained in detail
3. What is the input we get from "Car Products"?
- GD&T
- PART LISTS
- 3D CAD FILES
- CLAMP PLAN
- PRODUCT ASSEMBLY PROCESS SHEET
- GD&T
- GD&T -Geometrical Dimensional & Tolerance
- It provides information on locating pins, Rest, clamp, damp & Slide unit information of each station Also includes the information od sequence of openings of clamps, dumps & Slide stroke information.
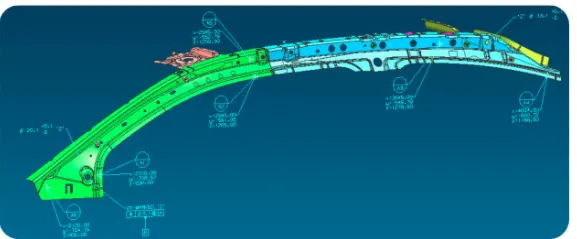
Fig GD&T input for a car product
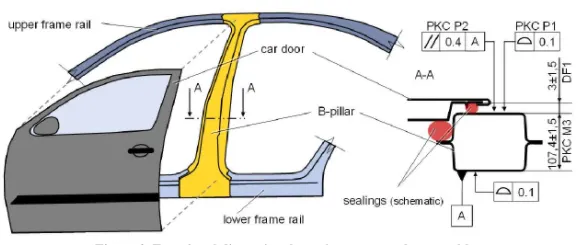
Fig functional dimensional requirements on the assembly
Some examples related to the inputs we get the GD&T in the car products are shown below
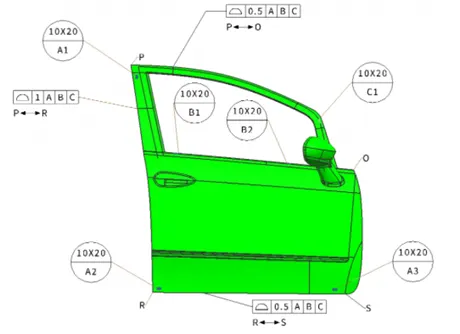
Fig car door with surface profile tolerance to ensure optimal assembly
A surface profile tolerance zone is a three-dimensional volume establishing a permissible boundary of features(s) of a part. A surface profile tolerance can be used to define a tolerance zone to control combinations of sizes from the orientation and location of a feature relative to the true profile. For additional information about profile tolerance, please refer to the section of the ASME Y14.5-2009 standard. we can observe the car door part location through datum targets with surface profile tolerances. in the next section, we shall analyze these tolerances further to better understand their functions.
Surface Profile tolerance along the left side of the door
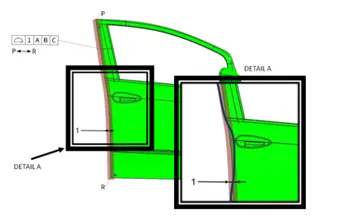
Fig surface profile tolerance zone between point P&R(Along the left side of the door)
Define by the red zone, in detail view, a close up showing the actual profile in dark blue
As shown in the above fig the surface profile tolerance zone between P&R along the left side of the door) must lie with the profile boundaries1mm apart (defined by the red zone ) and equally disposed about the true profile (0.5 mm on each side).thus features must be located within the tolerance zone 1mm relative to the datum reference frame ABC.in detail view. we can observe the actual profile of the door staying within these boundaries.
Surface Profile Tolerance Along the Top and Bottom sides of the Door:
The surface profile tolerance zone on the other edges of the door follows the same logic applied above
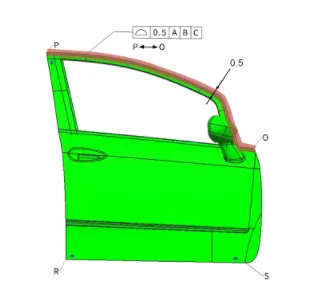
Figure. Surface profile tolerance zone between points P & O (Along the top side of the door)
As shown in above Figure 5, the surface profile tolerance zone between points P and O (along the top side of the door) must lie with the profile boundaries 0.5 mm apart (defined by the red zone) and equally disposed about the true profile (0.25 mm on each side).
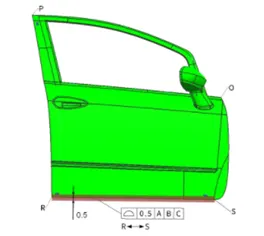
Figure 6. Surface profile tolerance zone between R & S (Along the bottom side of the door)
Lastly, in Figure 6, the surface profile tolerance zone between points R and S (along the bottom side of the door) must lie with the profile
boundaries 0.5 mm apart (defined by the red zone) and equally disposed about the true profile (0.25 mm on each side).
ii. Part lists:
- It gives the lists of parts that are going to assemble in the fixture.
- The list contains the information of Part number, part name, Revision of fixture, part thickness, etc. Damage result for Part lists
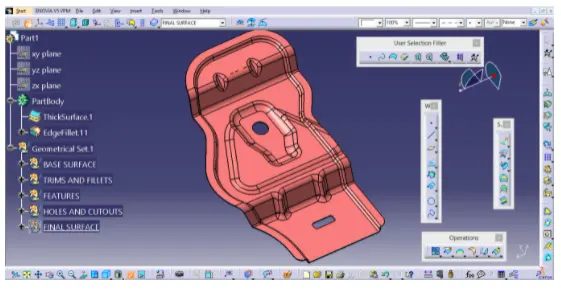
iii. 3D cad files:
The 3D model of the car part will be given to the customer. From that 3D model, we will be developing our fixture design process. The 3D cad file will be in the format of Step file (stp.) or IGES file (igs.) or sometimes it may be in a part file (part.).
 vi. Clamp plan:
- The clamp plan provides information on the location of pins, Rest units, clamp units, Dumps, etc.
- It is the important input from customers. The clamp plan/position should not be changed without the knowledge of customers. It gives the detail of the exact position of the clamping units.
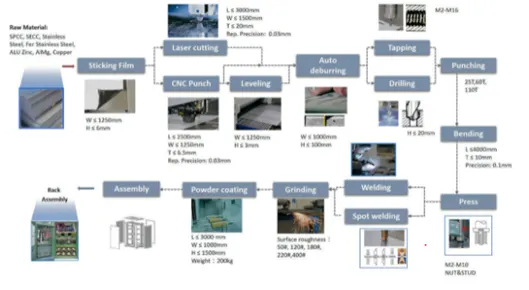
v. Product assembly process sheet:
- It gives the information of stage-wise assembly process like how the parts move from one assembly station to another after the completion of the joining process. It shows the sequence of operations/processes to be done in a part of a panel.
- Also what is the parts to be joined with the panel will show in sequence.
- From this sheet, we can trace out the pending process which has to further go on for completion of part. From this product assembly process sheet designer can understand the sequence for designing the fixtures.
Hence the inputs we get from car products are explained in detail
4. What is the Clamp plan?
CLAMP:
A clamp is a fastening device used to hold or secure objects tightly together to prevent movement or separation through the application of inward pressure.
Essential requirements of clamps:
All clamps must fulfill four essential requirements. They are,
- The workpiece must be held rigid while undergoing operations.
- The time required for loading/unloading the tool must be as short as possible, which means the clamping device must be quick-acting.
- When subjected to vibration, chattered, heavy pressure the clamping must be positive.
- The clamp must not damage the workpiece.
CLAMP PLAN:
- The clamp plan provides information on the location of pins, Rest units, clamp units, Dumps, etc.
- It is the important input from customers. The clamp plan/position should not be changed without the knowledge of customers.
- It gives the detail of the exact position of the clamping units by mentioning coordinates in the particular position.
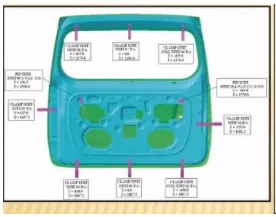
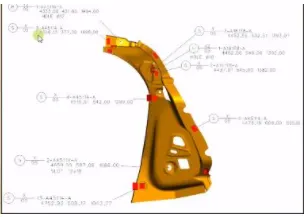
Fig Clamp unit
Hence the clamp plan is explained in detail
- What is the purpose of a Layout?
The purpose of the layout
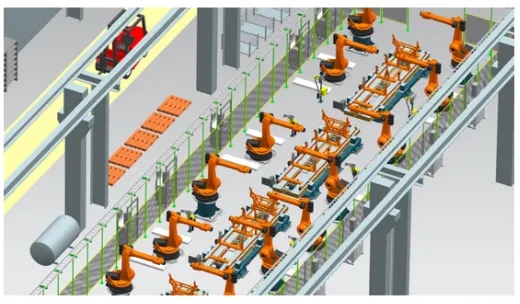
- The purpose of the layout is to understand the information about where the fixture &robots are been placed, the working area covered by the robot, what are the fixtures assigned for the robots to do the process, etc.
- The layout shows the entire assembly plan to understand the process
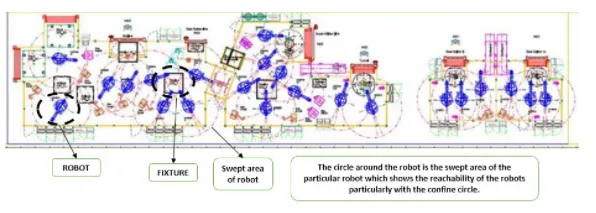
- The circle around the robot is the swept area of the particular robot which shows the reachability of the robots particularly with the confined circle
- The layout provides the information of flow of part, station pitch, robot station, accessories like tool changers & tips dressers, sub-assembly links, platform height, loading /unloading sequence/height
- The flow of parts: its shows the flow of the parts/panel in the assembly line or shop floor like how component move from one station to other station after the completion of the process
- Station pitch: the distance between two stations is known as station pitch, it shows the space contains between the two stations which show in the layout
- Robot Stations: It shows the positions where the robots & their accessories are placed, which is shown in the layout
- Sub-Assembly: sub-assembly link is nothing but the links between the assembly fixture & the main assembly line.it shows that how the subassembly fixture is linked with the main assembly line
- The main purpose of the layout is to understand the entire plan of an assembly line
- The layout providing the above information’s like the flow of parts, station pitch, robot station, etc used to understand the working process of root what are fixtures assigned for the robots, space constraint, etc
- By considering the layout, the design can develop the concept sketches of fixtures without any clash in the assembly line
- One of the main purposes is we get information about the space to constrain which helps to develop the robotic cell without any clash during working.
Hence the purpose of the layout is explained in detail.
6. What is Ergo data?
Ergo data:
Ergo data is nothing but the data or inputs which give the human factors engineering data, between the operation & his working environment. before detailing. Before detailing ergo data we should know about ergonomics in detail.
ERGONOMICS:
Ergonomics also known as human engineering & human actor engineering is the scientific study of the relationship between man and his working environment
Objective of Ergonomics
- The function objective of the study of ergonomics is to optimize the integration of man & machines to improve productivity & accuracy.
- In short, the objective of ergonomics is designing for human use & optimizing working & living condition
- Two broader objectives of ergonomics are
- To enhance the efficiency and effectiveness with which the work is carried out to increase the convenience of use, reduce error & increase productivity
- To enhance certain desirable human values including safety reduced stress fatigue, and improve quality of life
Ergonomics involves the design of
- A workplace suitable for the worker
- Machinery & controls, to minimize physical strain on the worker to enable the improvement in the efficiency
- An environment for performing a task most effectively and conductive
- A conducive task & work organization
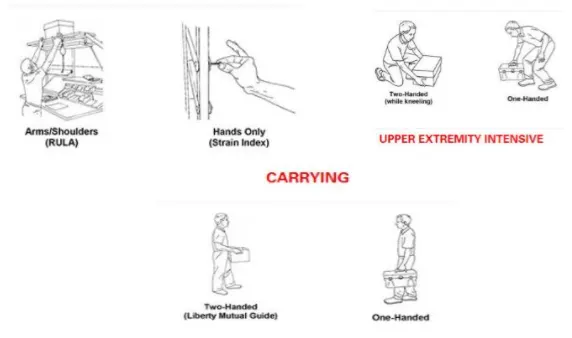
Benefits of Ergonomics
- Improve working condition
- Reduce physical workload
- Improve work postures
- Reduced efforts of certain movements
- Better reading instrument displays, handling of machine levels & controls
- Reduced unnecessary information recall efforts.
Below, I have given a basic example of ergonomics in the workstation
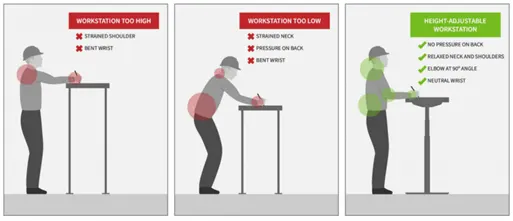
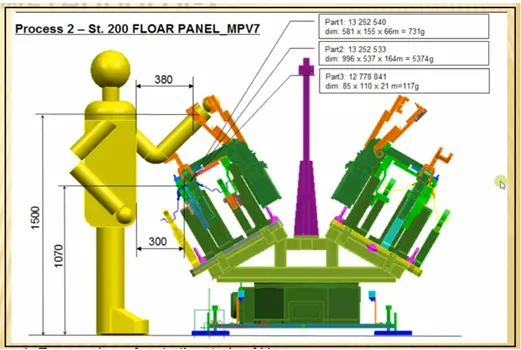
Fig 2 Example of Ergonomics in workstations
ERGO DATA:
- Ergo data is nothing but the data or inputs which give the human factors engineering data, between the operator & his working environment.
- Ergo data is most needed while there is a need for manual operator/operation.
- Ergo data will be given from customers as per their standards. Every customer follows different ergo data standards.
- As per customer standards, we have to consider the ergonomics in the fixture while designing. • From ergo data we get the details or inputs related between the operator and his working fixture.
- The Ergo data is mainly used to make the operator comfortable which may lead to improved efficiency in cycle time & production.
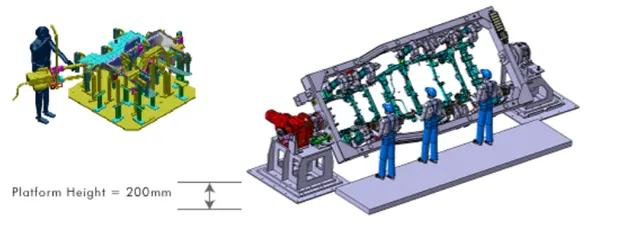
Fig Ergonomics in Fixtures
As shown in the below fig while loading & unloading the panels the approach of the operations from the fixture should be made easy in the manual fixture
Ergo data gives such inputs to consider with designing the fixture
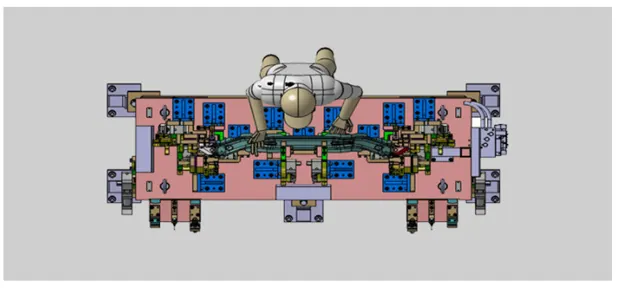
Fig shows the easy approach for the operators
- While loading & unloading the panels the approach of the operator from the fixture should be made easy in manual fixtures. Ergo data gives such inputs to consider while designing the fixture
- Ergo data provide inputs like Platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading.
- Also provides information like Loading height, working safety zone of an operator, etc.
- Mainly the ergo data is to make the operator comfortable like Visual check of the part, too much bending may get backbone pain or shoulder sprain for the operator which may tend to consume time & affect the efficiency of production.
- Ergo data is also needed to make the operator more efficient & timing saving. Also helps to improve productivity.
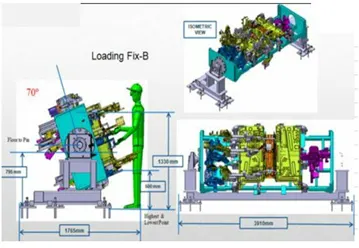
Fig the inputs given in the Ergo data
7. What do you understand by Weld's study?
WELD STUDY;
- Weld study is the important inputs from the customer.
- It gives the study of a particular gun that we use for the weld. No. of spots to be welded, Sequence of weld, the position of weld in the components.
- In short, Weld study includes weld gun details, weld matrix & weld points
- Generally, the weld points will be given in spheres. Red Sphere represents the Geo spot weld points whereas Green sphere represents the Respot weld paints
- The weld points are classified as
- Geo weld points.
- Respot weld points:
- Geo weld points:
- The Geo weld points are which is planned in the c 5 fixture
- . This weld will determine the position of the panels as per the given data in the drawing
- The Geo weld points are represented in red spheres in the weld study inputs given by the customers.
- Respot weld points:
- The Respot weld points are planned in the Respat tool.
- This weld will determine the strength/stiffness of the panel/components.
- The Respot weld points are represented in green spheres in the weld study inputs given by the customers
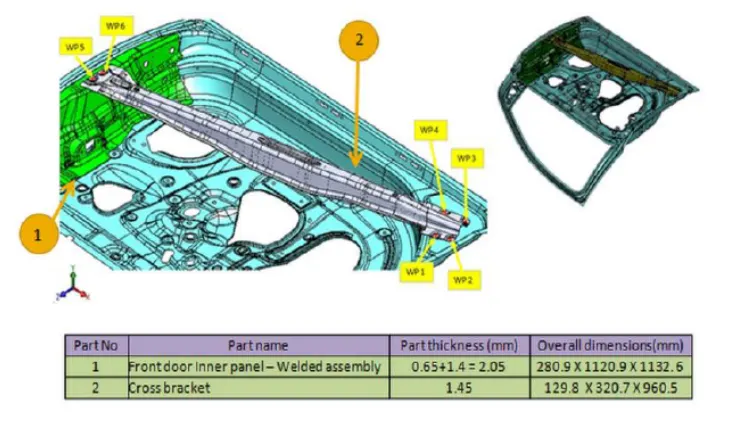
Fig Weld study
8. What are the criteria for percentage completion in the designing stage? Explain it in detail
THE CRITERIA FOR PERCENTAGE COMPLETION IN THE DESIGNING STAGE:
- The percentage completion criteria are followed in the designing stages & dispatch stages of welding fixtures
- This percentage completion criterion is followed to trace the project whether it matches the committed date given to the customer for handover the projects to them.
- Also, it helps us to identify the stages in the projects like how much the project is completed and what are the further stages are in pending to complete which helps us to complete the project on the committed time and date.
- The percentage completion criteria are divided into four stages to identify the percentage of the completion of work.
- The four stages of percentage completion criteria are as follows.
- Input & concept design.
- Concept approval & simulation check.
- Design freezing & detailing,
- Check & final dispatch.
- Input & concept design:
- If the project is in the stage of Input & concept design then the percentage completion criteria of the project will be between 0-25%
- After the completion of input & concept design then the project will be moved to concept approval & simulation check which is the second stage in percentage completion criteria.
- Concept approval & simulation check:
- If the project is in the stage of Concept approval & Simulation check then the percentage completion criteria of the project will be between 25% - 40%
- After the completion of concept approval & simulation check then the project will be moved to Design freezing & detailing which is the third stage in percentage completion criteria.
- Design freezing & detailing:
- If the project is in the stage of Design freezing & detailing then the percentage completion criteria of the project will be between 40% 85%
- After the completion of design freezing & detailing then the project will be moved to check & final dispatch which is the fourth & the last stage in percentage completion criteria.
- Check & final dispatch:
- If the project is in the stage of Check & final dispatch then the percentage completion criteria of the project will be between 85% 100%
- After the check, the project will be finally dispatched successfully to the customer.
Hence, the criteria for percentage completion in the designing stage are explained in detail.
9. Brief about "Output" in design?
- It includes data to be given to customers after completion of the design stage. the inputs are 3D models & 2D Drawings of the tools.
- In the fixture elements design output contains detailing of locators, detailing the design of clamps detailing of design od supports, positions of locators, positions of clamps, positions of support if any type of locators, type of clamps types of support, clamps forces & support
- There are two types of tools in the fixture design unitized tools & non unitized & non unitized tools
In unitized tools there are multiple units on common basic for e.g Geo fixture, respot fixture, checking fixture, hemming station, etc. unitized tools required two types of key sheet & layout sheet.
non-unitized tools that can stand alone & can be detailed completely on a layout sheet.e.g Rack,take out trolleys,turntables,grippers etc,
- Key sheet: an index of unit & their placement on the base of the tool, key sheet shows placement & location of that particular unit on tool base where the exact position of tools base key sheet is showing an orthogonal or isometric view of that entire component
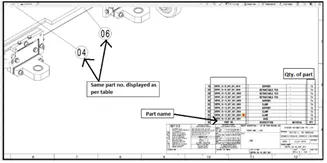
Fig: Key sheet
Layout sheet:-A detailed drawing of an individual unit to include all of their units layout sheet is a detailed drawing of that particular tool where we are going detailing of the component. The grid view below fig tells that where exactly the component is located in geometry. this is also helpful; in the CMM inspection of fixtures.
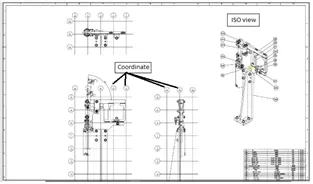
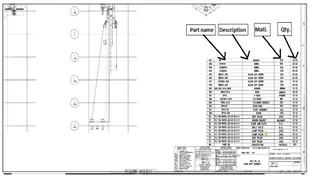
Fig:-Layout sheet
a). Approved standard parts should be used wherever possible. This saves lots of time, effort & economical.
- b) Design should be as simple & economical as possible. Geometry is complex then fixture design is complex but the approach is trying to design as simple as possible.
c). Design must comply with all current safety & ergonomics standard.
d). Design must provide for controlled & damage-free handling of the product. It should not damage the other part.
e). Adequate error-proofing provision must be incorporated in each design by providing proximity switches rough locators etc. Proximity switches are sensors that tell part is present or not in the fixture. Rough locators work as poka-yoke to guide the entire panel orientation f). The weight of the moving part must be kept to a minimum while maintaining maximum strength. Weight of moving component kept as minimum as possible but it shouldn't compromise on strength. There is a balance between these two things
g). Frames & structures are to be simple & sturdy
h). Design clearance & accessibility for routine maintenance & service. The fixture needs to maintain after a certain period so it is easily accessible for maintenance. () Motion control must be considered on any moving component. Adequate to control the motion of components like slider, clamp arm so that it does not give any vibration & stays on the particular limit by use of hard stopper, shock absorber. The designer is responsible to validate all clamps & weld guns. So that all clams & guns should perform their function without fail
10. What do you understand by structuring a design tree? How does it reduce errors during the design process?
STRUCTURING A DESIGN TREE:
Structuring a design tree implies a process where all the assemblies & parts are named in a specific standard. Different customers have different sets of standards to structure a design tree.
- It is an important process that helps us to identify a specific part or assembly as to which project, tool/unit, it belongs to This helps us to avoid errors during design study, manufacturing, assembly, inspection, etc.
- If the parts or assemblies are not named properly or the design tree is not structured properly, it will create confusion to understand the design & may create major possibilities of making an error.
- The naming of a fixture or a unit or a part gives the information as to which project or zone or assembly do they belong It can help us to identify the number of items of the same types or different types that are being used in the assembly. While start designing a fixture, the first unit will be the base unit.
- In the structure tree, all the manufacturing parts should be first and the standard parts should be at the last. A structure tree helps to study or understand the parts in the assemblies easily.
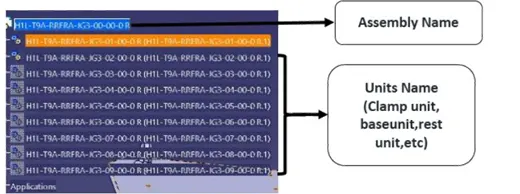
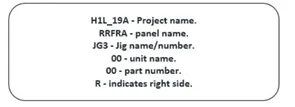
Fig design three structure (showing the sequence of naming procedure of assembly)
Steps of assembly structuring a design tree
- Step-1 create new product click on 0k (by clicking on ok you will enter into a product window)
- Step-2: The right-click product in a structure tree go to properties and rename in the part number( as we created a product we have a mention the total assembly name of the fixture) click Ok
The naming of the assemblies/parts/units has certain standard procedures, which I have clearly explained below.
The product name is the title of the fixture. The renamed title should be P001_Z03 T09_00_00_R
PO01-represent the project name.
Z03-Zone name
Pannel's name will also be mentioned in some cases.
ST 09-Station name/103-lig name will be mentioned sometimes.
00-unit name
00-Part number.
R/L-is represents the Right-hand side / left-hand side of the panel
The other renamed title explained in the video is HIL_19A RRFRA JG3_00_00_R
HIL 19A-Project name.
RRFRA-panel name
IG3-ig name/number
00-unit name
00-part number
R-indicates right side.
Thus this is how the assemblies have to be mentioned in a sequence of procedure
- Step 3: Insert new component (under project title) Click the newly created component and rename it as we have done in the before step
Example: POO 203 ST09-01 00 Base unit (Always the first unit should be a base unit in the structure free)
POO_Z03 STO9_02_00_clamp unit
01/02 - represent a unit
00-represent part
- Step 4: Repeat the same we did in the before steps to create various units like clamp unit, rest unit, etc. by creating a new component.
- Step 5: Insert parts (under the particular unit name) to add parts that consist of the units. And rename the parts as we did usually in the before steps.
Example: POO_Z03-ST09_02_01_Clamping mylars
POO_Z03-STO9_02_02_Clamp Arms.
Here. 01 - represents part01 (clamp mylars) in unit 02 (claiming unit) whereas 02 - represents part02 (clamp arm) in unit 02 (claiming unit)
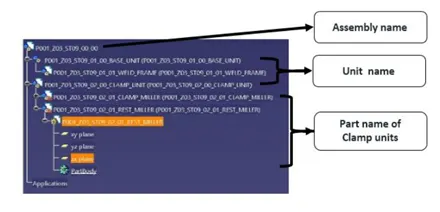
Fig:- Design tree structure (showing some of the parts under the clamp unit)
- Step:-6:- To sketch a part in a sketch unit click a part name in a structure tree (which part is to be designed ) & then go to the new part window. now the part window in the selected part name on the structure tree will open. then by selecting the sketch and various tools we can design a particular part in the units
- Step:-7The Step-6 has to be repeated for creating all parts under different units
- Step:-8 The standard pats should be mentioned at last /mentioned after all the in house manufacturing parts should be mentioned at the; last /mentioned after all the in house manufacturing parts in the design structure tree
- These are the simple steps to be followed to structuring a design tree.
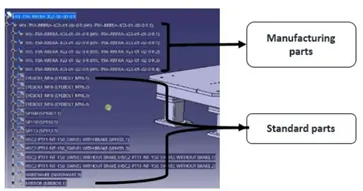
Fig Design tree structure (Showing procedure of positioning the manufacturing & standard part in a design tree)
Hence, structure a design tree is explained in detail with the point of how it reduces error during the design process
11. What are Units? Mention 5 types of units.
Units
- In general, a unit is a device that has a specified function, especially one forming part of the complex mechanism
- A welding fixture is an assembly of different types of units
- As the name refers, the different units will be only seen in the unitized tool
- Units are classified into two, they are
Units are mainly divided into two types
- Unitized
- Non -unitized
- Unitized tools
Unitized tools are tools that are a part of multiple tools inside of it
These are the tools that have to be represented by two formats key sheet and layout sheet
Unitize tools are two types
- Simple units and
- Complex units
- Non-Unitized tools
Non-unitized tools are one unit itself, which is don’t have any processing functionality it is just to keep component on it as a sable, like grippers turntable stand, etc.
- Simple unit: in a simple welding fixture, the combination of these different units will be seen
- Rest unit
- Fixed pin unit
- Retract pin unit
- Rough locator unit
- Sensor unit
- Base unit
- Complex unit: in a complex welding fixture in addition to some of the simple units these complex units will also be seen
- Slide unit
- Dump unit
Below I have mentioned 5 types of units
- Base unit
The base unit is the unit designed to mount all other units such as clamp units, pin units, rest unit, etc., of a tool like pneumatic value box, trunking cable path will also be mounted on to be a base unit
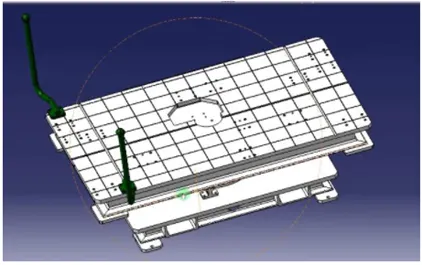
Fig 1. base unit
2. Fixed pin unit
- Fixed pin unit is a unit designed to locate the car panel using pins
- Pin, pin retainer, shims, blocks, blade, riser are the part of the fixed pin unit
- Pin retained is used to hold the pin firmly
- Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process
- The body part is constrained by a set of appropriately locating pins so total constraint by locating pin should be fully constrained at all times to prevent any movement
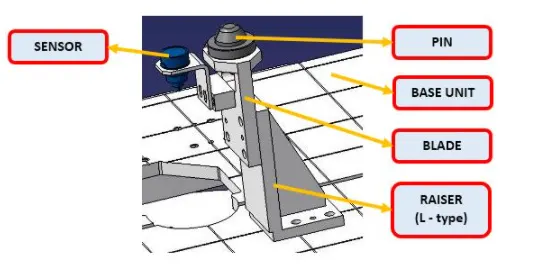
Fig pin unit attached with sensor
3. Retractable pin unit
- A retractable pin unit is a unit designed to locate the car panel using pins but the entire pin package parts will be mounted on the retractable pneumatic cylinder as shown in below fig
- Retractable pin unit is the opposite of fixed pin unit which can move up& down also which can be retracted till certain distance
- It is mainly used for unloading the complex panel after welding
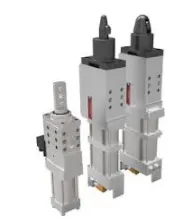
Fig Retractable pin unit
- Clamping unit
- A Clamp unit is a unit designed to clamp or hold the car panel with NC block/ mylars by using a pneumatic clamp cylinder
- A clamping unit is used to clamp the part which is to be welded after location using a pin unit
- Clamping is achieved with the help of a pneumatic cylinder and clamp arms
- Clamp arm, finger, rest, shims, standard riser, pneumatic cylinder are the parts of clamping units in general
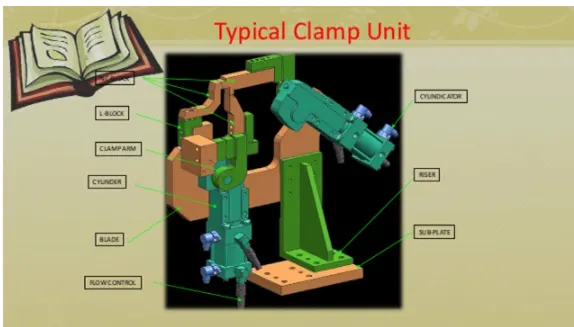
5. Slider unit
- Slide unit is found mostly in the complex fixtures, where the sliding mechanism will be involved.
- This type of unit is used when there are some space constraints.
- Guide block, guide rail, position lock unit, stopper block. sensors are the parts of the slide unit in general. Guide block & guide rail helps to guide the slide unit. The rail should always be covered to protect against weld spatter & dust by a bellow or a sheet metal cover.
- Position lock unit helps the slide to be lowed/clamped in the working position.
- stopper block helps to stop/control the entire moving of a slide unit from a certain distance, which is placed at the end of the guide rail.
- Sensors - The two end limits to be sensed externally by a proximity sensor.
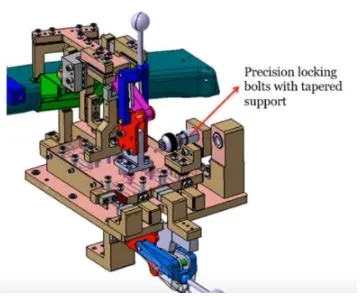
Fig slide unit
12. Describe Fixed Pin units & their purpose?
Fixed Pin Unit
- Fixed pin unit is the unit designed to locate the car panel using pins
- Pin, pin retainer, shims, blade, riser, are the parts of fixed units in general.
- Pin, a retainer is used to hold the pin firmly
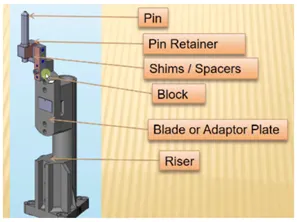
Fig Fixed pin unit
Purpose of fixed pin unit
- Based on the 3-2-1 locating principle, the induction of two pins helps to arrest the 6 degrees of freedom (4Axial &2 Radial movement) whereas the other 6 degrees of freedom are arrested by introducing a minimum of three supports
- Typically the locating pins are used to locate body parts in a position sufficient accuracy to execute a welding process
- The body part is constrained by a set of appropriately locating pins so total constraint by locating pins should be fully constrained at all times to prevent any movement
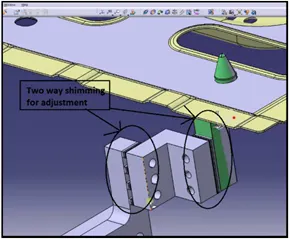
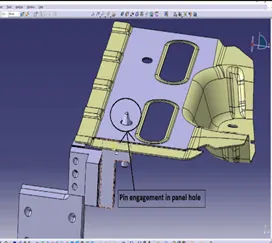
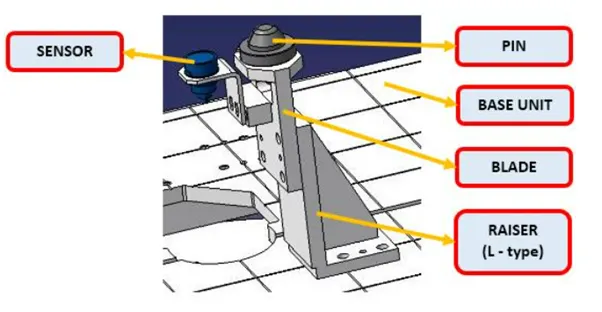
Fig fixed pin unit attached with sensor
13. What are the different parts of a fixed unit?
Different parts of the fixed pin unit:- the different parts of the fixed pin units are as follows
- Pin
- Pin Retainer
- Shims
- Blade
- Riser
- L-Blocks
- Pin
- It is used for the location purpose of the panel
- Typically the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process
- The body parts are constrained by a set of appropriately locating pins so total constraint accurate to execute a welding process
- The body parts are constrained at all times to prevent any movement.
- There are dozens of styles locating pins that can be utilized in a design. below I have shown the commonly used pins
One of the most common pins is a stepped pin with a wither small or large head
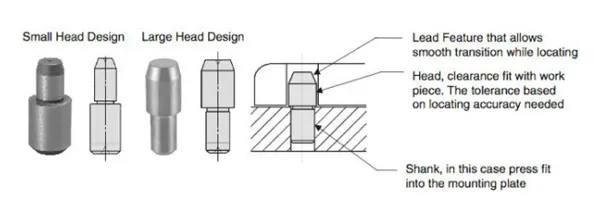
Fig locating pins
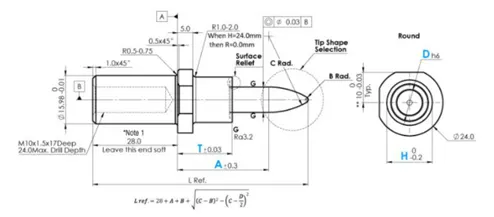
Fig NAAMS standard locating pin(6-way small head) make MISUMI2
2. Pin Retainer
Pin Retainer is to hold the locating pins firmly
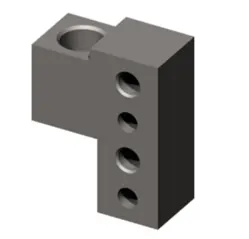
Fig NAAMS standard- pin Retainer(APR 336M)
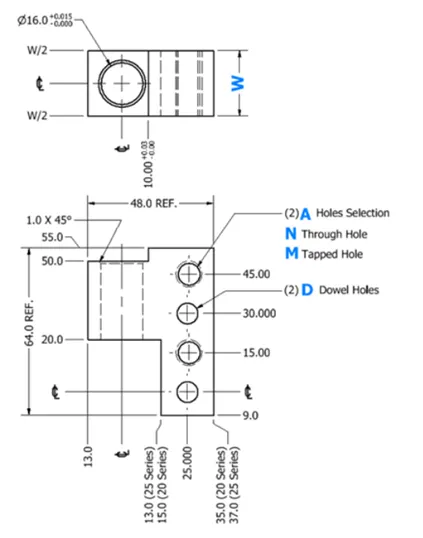
Fig NAAMS STANDARD -pin Retainer(APR L shaped 4-side holes)
3. Shims:
- In general, A shim is a thin and often tapered or wedged piece of material used to fill small gaps or spaces between objects.
- Shims are typically used to support, adjust for better fit, or provide a level surface.
- Shims may also be used as spacers to fill gaps between parts subject to wear.
- Shims are the small parts that come with the thickness of 0.1mm,0.2mm,0.5mm, 1.0mm, etc.
- These will compensate the stack up a tolerance which reflects at the mylars.
- We give tolerance to all parts of the fixture. Due to this tolerance, the mylars will either lift moves down from their defined position.
- To adjust the mylars for getting the defined position, we use shims.
- Shims will be added above the mylar for adjusting according to tolerance.
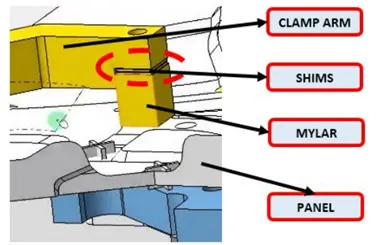
Fig shims
Applications of Shims
- In an automobile, Shims are commonly used to adjust the clearance or space between two parts, for example, shims are interested into under bucket tappets to control valve clearances, clearances are adjusted by changing the thickness of the shim
- In assembly and weld fixtures, precision metal shims are used between two parts so that the final production parts are created within production drawing specified tolerance
- Types of Shims
- Wood shims
- Stone shims
- Plastic shims
- Metal shims
- Paper shims
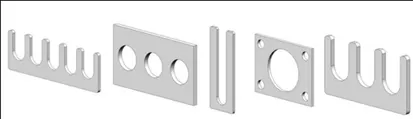
4. Riser
- The riser is a manufacturing part used to raise /height the assemblies of the Fixture
- One end of the raiser will be attached to the base unit while the other end will be attached to the blade
- Raiser can be two types, they are
- L type raiser
- Square type Raiser
- L-Type Raiser:
L-Type Raiser are of welded type .where the stiffener well be added at the center for support .as shown in the below figure the wedge-shaped structure is known as stiffener which is used as a support /to withstand the load
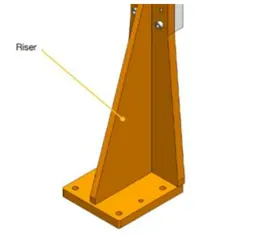
Fig L-Type Raiser
- Square tube Risers: Square Tube raiser
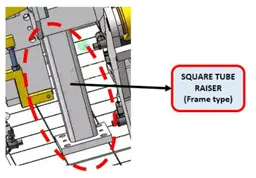
Fig 8 square type Rise(frame Type)
5. Blade
- The blade is the plates that are attached to the raiser
The blade is also attached or mounted with a cylinder, arms, etc
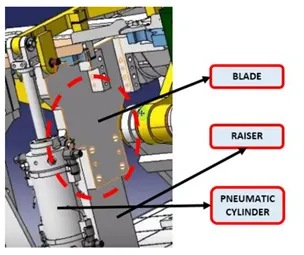
Fig Blad
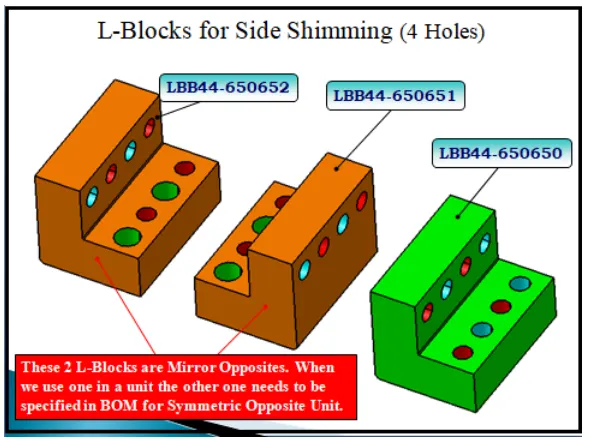
6. L-Blocks
L-Blocks are used just to provide the necessary shimming for the adjustment, in case of mounting an L-block, we should check to bolt access as there is already a bolt to tight the pin, hence a clear hole should give from L.Block.
14. What is the purpose of making a Rest unit & describe its parts?
Purpose of making a rest unit:-
- Rest unit is a unit designed for the purpose to rest/support the car panel using NC block or mylars
- The mylars in the rest unit are known as resting mylars.
- In this unit the part of the panel will be rested, it will not have clamps or force applied to it.
- Rest units consist of a few mylars, risers & blades.
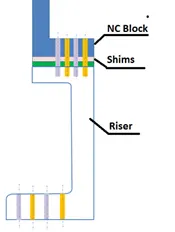
Fig Section view of Rest unit
PARTS OF REST UNIT: The parts of the rest unit are as follows.
NC block/mylars
- Risers
- Blades
- NC blocks/mylars
- Mylars are the part which is holding the panel from top & bottom.
- It is a jaw type, during welding it won't deform from its position,
- It is also known as fingers
- It doesn't allow the deformation of the part due to welding stresses.
- Mylars are of two types, they are
- Clamping mylars
- Resting mylars
- Only resting mylars can be seen in the Rest unit.
- The panel which rests on the part is known as Resting Mylars.
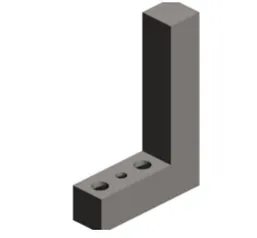
Fig NC Block or Mylars
- Risers:
- The riser is a manufacturing part used to raise/height the assemblies of fixtures.
- One end of the raiser will be attached to the base unit while the other end will be attached to the Blade.
- Raiser can be of two types. They are,
- L' type risers.
- Square tube risers.
- 'L' TYPE RISERS: 'L' type risers are of welded type. Where the stiffener will be added at the center for support. As shown in the below figure the wedge-shaped structure is known as stiffener which is used as a support /to withstand the load.
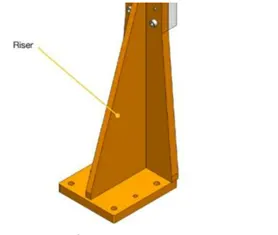
Fig L-type Raiser
Square Tube Raiser: Square tube raisers are of frame type
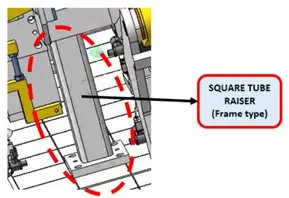
Fig square type riser(Frame type)
d.Blade
The blade is the plates that are attached to raise
The blade is also attached or mounted with cylinder arms etc
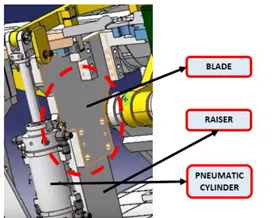
Fig Blade
- What are the fundamentals to design a Sensor unit?
Sensor Unit
A sensor is a device that measures physical input from its environment and converts it into data that can be interpreted by either a human or a machine. most sensors are electronics (the data I converted into electronic data), but some are more simple, such as glass thermometers, which present visual data, people use sensors to measure temperature, gauge distance, detect smoke, regulate pressure, and the myriad of other uses.
TYPES OF Sensors Used in General
- Proximity sensors
- Photoelectric sensors
- Laser sensors
Proximity sensors:
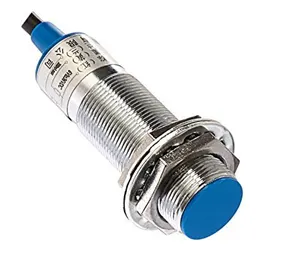
A proximity sensor is a non-contact sensor that detects the presence of an object when the target enters the sensor's field. Depending on the type of proximity sensor, sound, light, infrared radiation (IR), or electromagnetic fields may be utilized by the sensor to detect a target. Proximity sensors are used in phones, recycling plants, self-driving cars, anti-aircraft systems, and assembly lines. There are many types of proximity sensors, and they each sense targets in distinct ways. The two most commonly used proximity sensors are the inductive proximity sensor and the capacitive proximity sensor.
An inductive proximity sensor can only detect metal targets. This is because the sensor utilizes an electromagnetic field. When a metal target enters the electromagnetic field, the inductive characteristics of the metal change the field's properties, thereby alerting the proximity sensor of the presence of a metallic target. Depending on how inductive the metal is, the target can be detected at either a greater or shorter distance.
Capacitive proximity sensors, on the other hand, are not limited to metallic targets. These proximity sensors are capable of detecting anything that can carry an electrical charge. Capacitive sensors are commonly used in liquid-level detection.
Photoelectric Sensors:
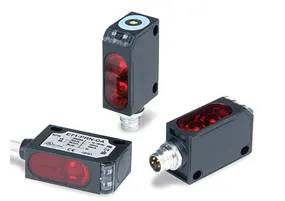
Photoelectric Sensors detect objects, changes in surface conditions, and other items through a variety of optical properties A Photoelectric Sensor consists primarily of an Emitter for emitting light and a Receiver for receiving light. When emitted light is interrupted or reflected by the sensing object, it changes the amount of light that moves at the Receiver. The Receiver detects this change and converts it to an electrical output. The light source for the majority of Photoelectric Sensors is infrared or visible light (generally red, or green/blue for identifying colors).
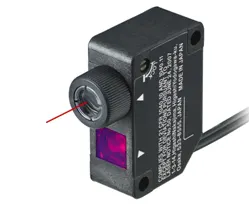
Laser Sensors: These laser distance sensors use a focused, coherent light to measure the distance to a target object. In factory automation applications, the target is usually a product or a machine element. They detect any solid object and produce an output proportional to the measured distance independent of material, color, and brightness. The high-resolution output provided by laser distance sensors is used to provide position or displacement, usually to the input of some type of industrial controllers, such as PLC. The output signal is often highly accurate, and it includes temperature compensation to enhance stability. There are several types of laser distance sensors including diffuse, background suppression, and retro-reflective. These sensors use CMOS or transit time technologies, providing accurate distance measurements Laser light must be focused, and it must stay narrow over a great distance and at a narrow spectrum (color of light). The emitted can then be triangulated or pulsed, with each pulse return measured to create distance readings.
Fundamental Of Sensor Design
- Every single loose panel, Which are being welded in the tool should be sensed
- Each panel should be sensed by one or two sensors depending on the size of the panel preferred to be in diagonally opposite end of the panel
- if a component is really small, We need not use two or three sensors for that you can use one sensor to detect the particular panel.
- If the panel is really big, we will use two sensors in opposite directions to sense the panel. so every sensor should be mounted in three directional adjustable ways in general.
- Sensor manufacturers are IFM,paper-Fuchs, OMRON
16. What is a Rough locator unit & what are the fundamentals to consider while designing it?
ROUGH LOCATOR UNIT
- A rough locator unit is a unit designed to guide the operator to locate the car panel onto the pins accordingly. A rough locator can be of standard parts or make part...
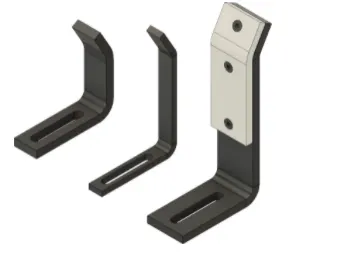
Fig:-Rough Locator (NAAMS standard)
THE BASIC FUNDAMENTALS TO CONSIDER WHILE DESIGNING A ROUGH LOCATOR:
- Rough locators should be placed at the edges of the car panel which has to guide,
- Rough locators should be placed at the same angle of the car part edge with a minimum distance of 2-5 mm from the edge of the car part.
- Rough locators should guide the panels in pin assembly direction in general
- Rough locators Start guiding the panel before 10 to 15mm to the start of the pin engagement,
- Rough locators should be designed with entry angle for car part entry as shown in the above figure 1 Rough locators should be designed with two slots to mount for easy adjustments in general
- The slots should be in the direction of the car part guiding
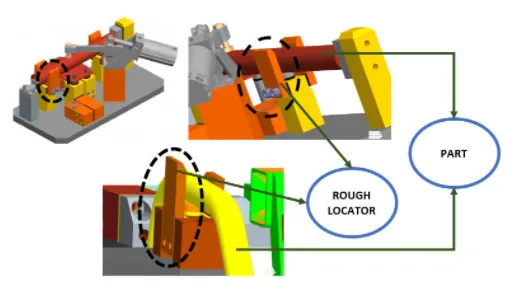
Fig Rough Locator
17. What is a Base unit and describe its parts?
A base unit designed to mount all the other units(Clamp unit, pin unit, etc)of the tolls, also other parts necessary for a tool like pneumatic valve box trunking cable path will be mounted onto a basic unit.
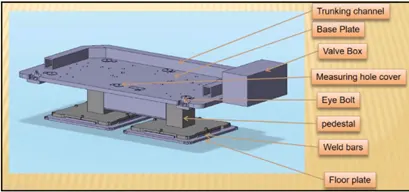
Fig base unit
PARTS OF BASE UNIT: Parts of the base unit are as follows
- Valve box
- Truncking channel.
- Measuring hole cover
- Eyebolt
- Pedestal
- Floorplates
a. Valve box
- A valve box is a box that supplies air to all the pneumatic cylinders assembled in the fixture Valve box consist of one solenoid valve with one inlet and one outlet. The outlet in the solenoid valve is used to supply the air to the pneumatic cylinders from the valve box Whereas, the inlet in the solenoid valve is used to collect the air from the pneumatic cylinders to the valve box
b. Truncking channel.
- Truncking channel is a kind of cable duct, which helps to guide and protect the wiring/tubes used in the fixtures
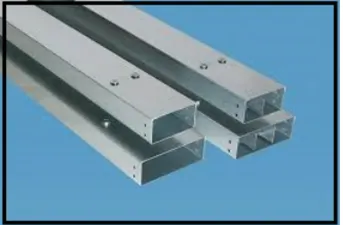
Fig Truncking channel
c. Measuring hole cover
- In the measuring hole cover, the coordinates points are engraved on it. The hole which mentions the coordinates gives the position & placements of the particular units.
- The measuring hole helps in CMM inspection & OC inspection
d.Eyebolt:
- An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it for lifting purposes.
- Eyebolt is used to drag or lift the base unit while relocating
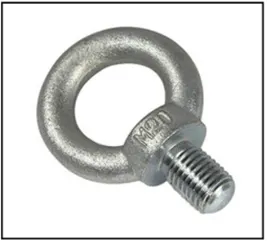
Figure 3. Eyebolt
e. Pedestal:
- The pedestal is a stand like structure where the entire unit of the base will be mounted
f.Floor Plates
- Floorplates are used to mount the entire base with the floor.
- Also, it helps to achieve the flatness of the future.
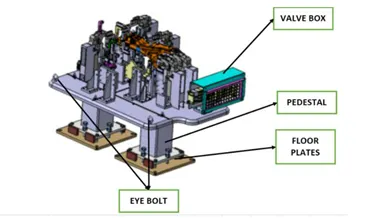
Assembly of fixture highlighting the part of the base unit
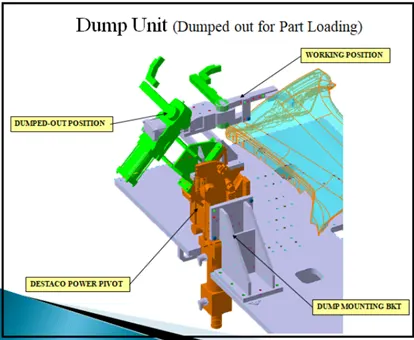
18. What is a Dump Unit and what are its functions?
Dump unit
- A dump unit is found in the complex fixtures.it is used when there are any geometrical constraints while placing a panel
- The dump unit consists of a dump cylinder to perform clamping &unclamping
Functions of Dump Unit
The dump unit plays a vital role when there are any geometrical constraints while placing a panel
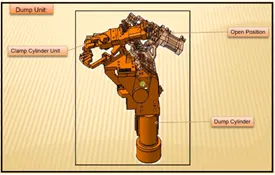
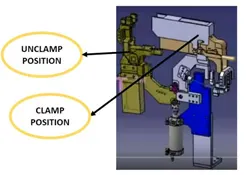
FIG Dump Unit
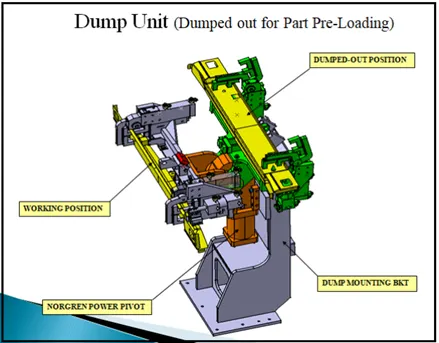
19 What is a Slide unit? Mention where Slide units are commonly used.
SiDE UNITS
- Slide units are positioning units, which are used to position the car part or panel. units weld gun, slots for further operations
- Slide units may be classified into two types based on the type of guideways they are,
- Handed guideway.
- LM guideways
- Slide units may be further classified into three types based on the prime mover. They are
- Manual slides
- Hydraulic/pneumatic slides
- CNC Slides.
- it may be further classified depending on the application as
- Horizontal slide unit.
- Vertical slide unit
- Angular slide unit
LM gade ways are preferred over hardened guideways due to the least coefficient of friction
ESSENTIAL PARTS OF SLIDE UNIT
- Slide unit essentially consists of guide blocks, guide rails, position lock, stopper block sensors. linear cylinders
- Guide block & guide rail helps to guide the slide. The role should always be covered to protect against weld spatter & dust by a bellow or a sheet metal cover Guideways to be lubricated for long life
- Position lock -unit helps the slide to be locked/lamped in the working position.
- Stopper block- helps to stop/control the entire moving of a slider unit from a certain distance, which is placed at the end of the guide rail.
- Sensors -the two end limits to be sensed externally try a proximity sensor
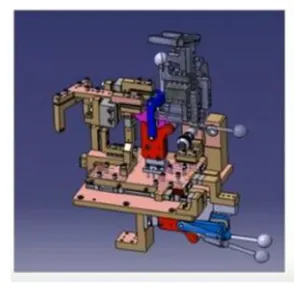
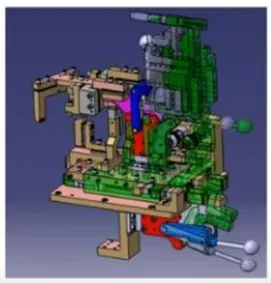
Slide-in Working Position Slide-In Retracted Position
Fig Slide unit in working & Retracted position
Fundamentals of slide unit design:
- Reverse stroke of 10mm to be considered in both forward & retracted conditions.
- Cylinder & LM guides to be validated for load & stroke.
- LM guide rail length should be standard & should be more than the actual stroke.
- Master guideway should be constrained & the subsidiary guideway to be free.
- Mechanical hard stop to be considered for both extended & retracted conditions.
- Shock absorber should be used for both extended & retracted conditions to reduce impact load. Slide to be locked/clamped in the working position.
- Slide to be locked with a safety pin in the retracted position during transportation.
- The two end limits are to be sensed externally by a proximity switch.
- The LM rail should always be covered to protect against weld spatter & dust by a bellow or a sheet metal cover.
- The design should be checked for screw accessibility, ease of assembly, machinability of parts.
- The LM guide & rails are integral assemblies and should not be separated at any cost.
- The shock absorber should be mounted such that it is perpendicular to the pivot at mid-stroke or within +/- 5 degrees.
- LM guideways to be lubricated for long life.
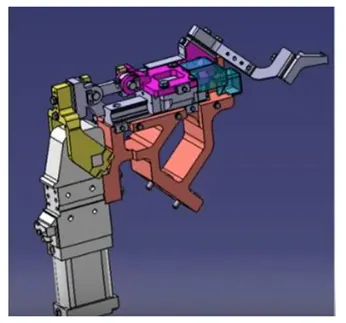
Fig Slide unit shows an alternate method of designing a guideway
Slide Unit Are Commonly Used In
- The slide unit is found mostly in the complex fixture, where the sliding mechanism will be involved.
- This type of unit is used when there is some space constraint in locating the panel
- Slider application will be easy for welding
- Slider unit can minimize the cost of the robot as slide unit provided to move weld from one weld spot to another weld spot instead of weld robot
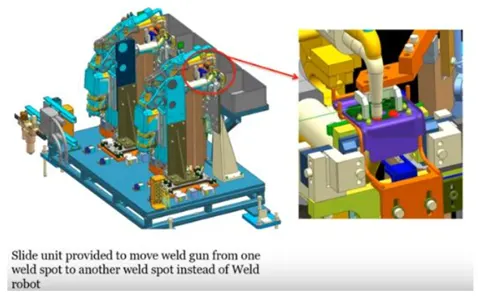
Fig Slide Unit