Week 3:- BiW Fixture Design Methodologies Challenges
Week 3: - BiW Fixture Design Methodologies Challenges
Q1. What is Design Methodology?
Ans. Design methodologies are the steps that are followed during the concept designing stage of the fixture.
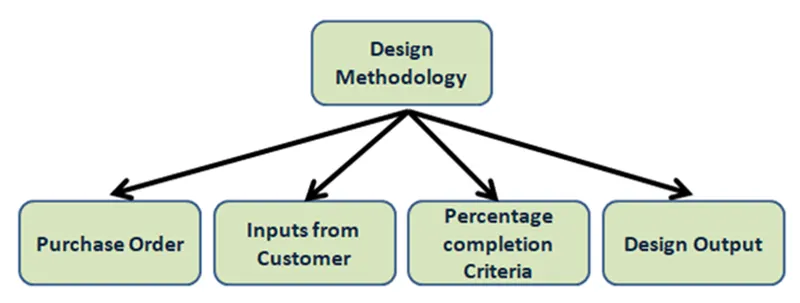
Design Methodology is divided into four Sub categories:
Purchase Order
Inputs from Customer
Percentage Completion Criteria
Design Output
Purchase order: Purchase order is the confirmation from the customer side that we are ready to start. It is the official document received from the customer. which commits the customer to pay the seller for the sale of a specific product to be delivered in the future.
Input from customer: Inputs from customer are major input that we get from customer. We study those input to what kind of information get out of it.
Percentage Completion Criteria:
Percentage completion criteria is basically schedule that till what time that we can complete the entire process. So when we are going to complete the in entire designing, then we're going to move on to simulation on all these subcategories would be considered in percentage completion criteria like a probability to when we can complete the entire fixture design.
It is followed in the designing stages & dispatch stages of welding fixtures. It helps to track or identify how much task completed & how much to go further for completing a fixture.
Inputs & concept design – 0 to 25%
Concept approval & simulation check – 25 to 40%
Design freezing & detailing – 40 to 85%
Check & final dispatch – 85 to 100%
The above-mentioned percentage are the percentages of stage wise completion criteria of the projects.
Design Output:
Output consist of 3D models, 2D drawing which is the detailing part, BOM & other related documents.
Q2. What are the inputs required from the customer to start designing a Fixture?
Ans.
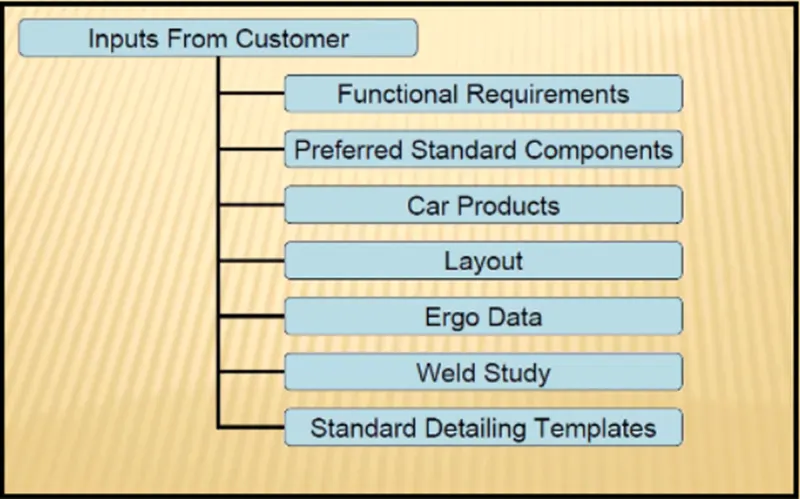
Inputs from the customer includes:
- Functional Requirements: It is the place which tells that what functions are to be required in the process, e.g., welding, gluing etc.
- Preferred standard components: Every industry has its own standard & they follow that standard. In this requirement, preferred standard component is basically what kind of standard component customer already has. Standard like ABB, NAAMS, FAUNC, FESTO, TUNKERS, ZYTRAN, DESTACO, Siemens etc. are used for robot, pneumatic parts, motor & gearbox, electric parts.
- Car Products
The inputs regarding GD&T, part lists, Clamp plan, Pin Locating Points, Product assembly Process Sheet are received by car products.
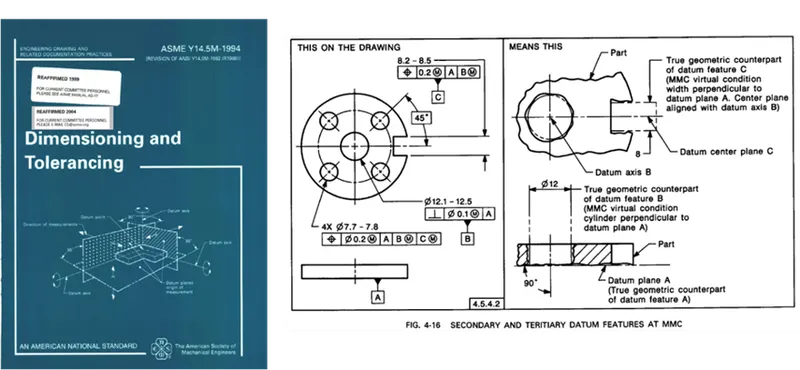
GD & T: It gives information about the location of pins, Rest, clamps, and slide unit information of each station.
- Parts lists: It gives information of part like part name, the part number of the part which is to be assembled in the fixture.
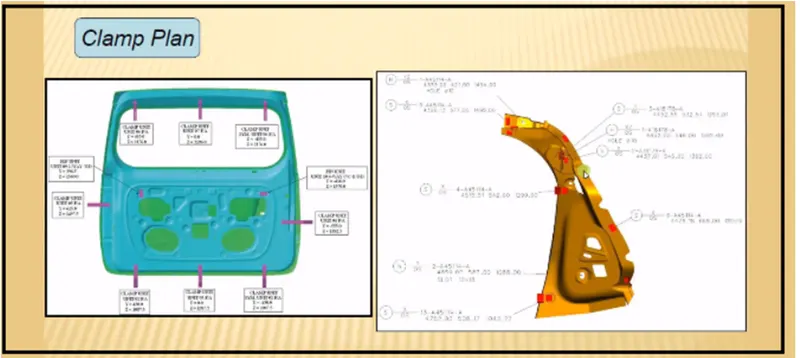
- Clamp Plan: Clamp plans give the location of pins, rests, clamp, dumps, etc. we need to consult with the customer if we need to make changes in the clamp plan.
- Product Assembly process sheet: It gives details about the sequence of the assembly of parts in the various stations.
- CAD Files: The 3D model of the car part is required for designing the fixture for that part.
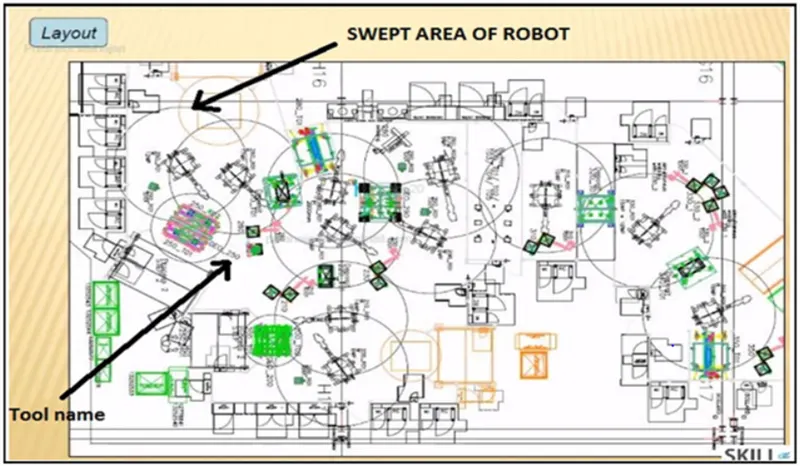
- Layout: The layout provides information about the flow of the product, assembly sequence, the position of robots, sub-assembly links, accessories like tool changer and tip dresser, platform height.
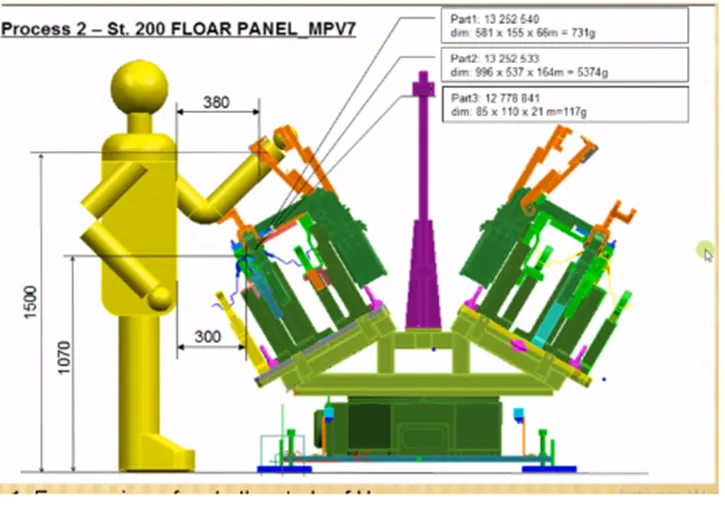
Ergo data: We have to follow the customary standards of ergo data. The inputs of Ergo data will be given by the customer mostly in case of manually operated fixtures. The Ergo data is mainly used to make the operator comfortable which may lead to improve the efficiency in cycle time and production.
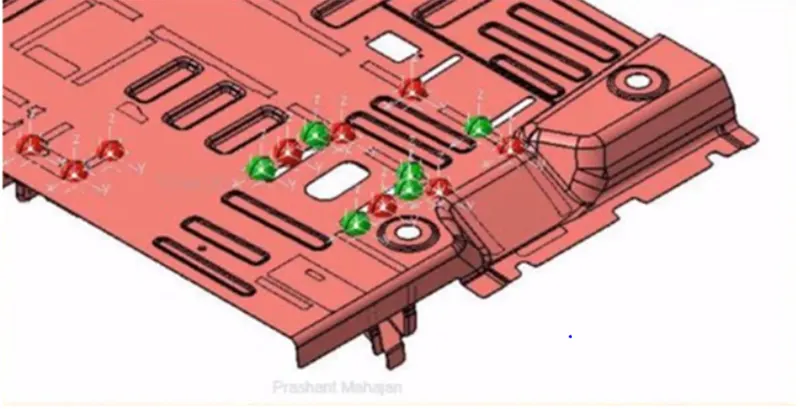
Weld Study: Weld study gives information about the type of weld gun to be used for the process. Also, it gives information about the number of geo weld spots as well as the number of Re-spot welds. These spots will be indicated using red and green spheres respectively.
3.What are the inputs we get from "Car Products"?
Ans. The inputs that we get from the care products are as follows:
- GD&T
- Part Lists
- CAD Files
- Clamp Plan
- Product Assembly Process Sheet.
GD & T stand for Geometrical Dimensioning and Tolerance. GD & T of each part is given in car product in which information of locating pins, clamps, rest and slides are mentioned.
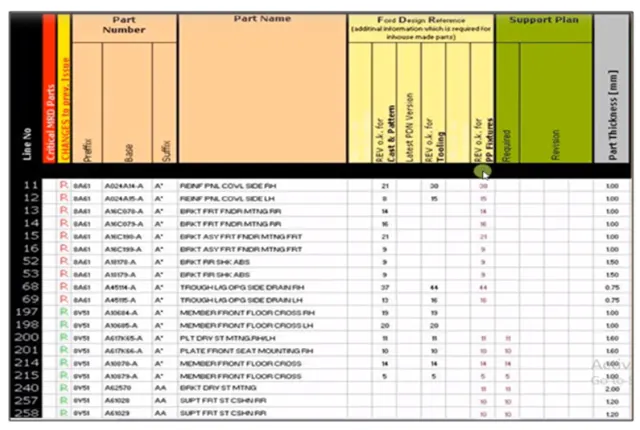
Part List: Part list gives thee information of parts in a unit.it consists of part number, part name which helps to identify the part easily, number of parts required and its thickness. This list helps to check all the parts and its dimensions and required number of quantities.
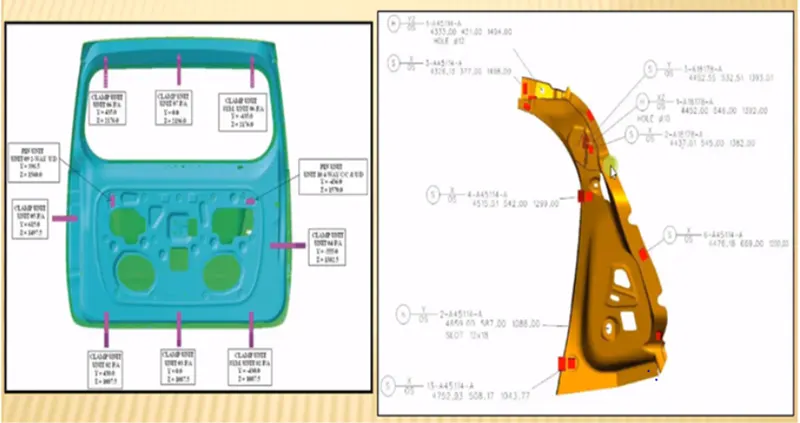
CAD Files: The 3D model of the car part is required for designing the fixture for that part. CAD files of car parts gives the simulations of those 3D models and their analysis. It is also used throughout the engineering process from conceptual design and layout of products
Clamp Plan: Clamp plans give the location of pins, rests, clamp, dumps, etc. we need to consult with the customer if we need to make changes in the clamp plan.
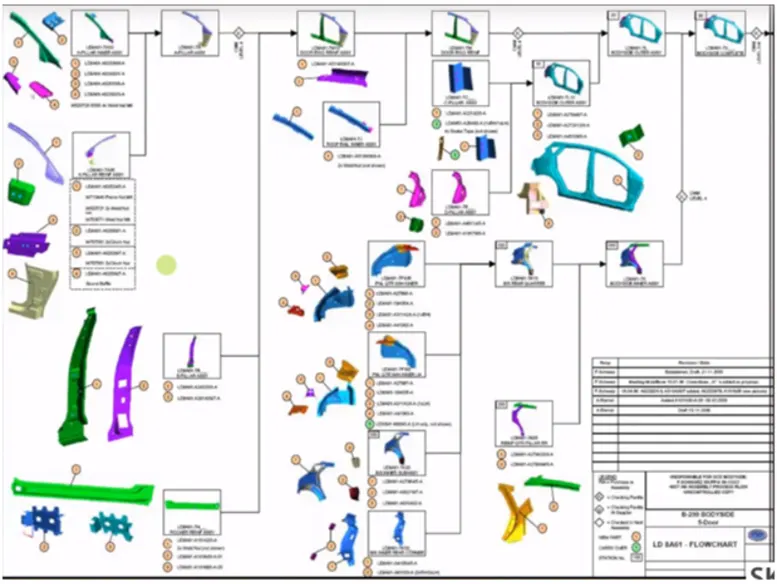
Product assembly process sheet: It shows how the product is going to move from one assembly station to another and provides information about which part to be assembled at which stage.
No changes can be made in the assembly process without consultation with the customer. Product assembly process sheet gives complete assembly of a unit. Different parts in a unit are assembled by geo weld first. Then the weld parts are assembled by re-spot welding.
Q5. What is Clamp plan?
Ans. Clamp plan provides the information of location of pins, Rest units, clamp unit, Dumps etc. It is the important input from customer. Clamp Plan is a document that contains the panel drawing mentioning all the places where clamps and rests are to be given. It gives exact location in X, Y, Z co-ordinate values to start designing. We should never change clamp position without permission of customer. Clamps are nothing but a mechanism or component used to hold or clamp job in fixture securely. Clamps are manual type, hydraulic type or pneumatic type depending on customer requirement. Clamp plan mentions or gives the location of clamps in which component is going to clamp.
A clamp is a force-actuating mechanism of a fixture. The forces exerted by the clamps hold a part securely in the fixture against all other external forces. Clamping surfaces are subjected to the clamping forces for obtaining invariant location. To fix a part at a particular position, we use 3-2-1 principle in all types of fixtures to restrict degrees of freedom. Each Panel is fixed keeping 3-2-1 principle in mind. This principle requires us to use minimum 3 rests, 2 pins and 1 clamp to fix a panel
Q5.What is the purpose of a layout?
Ans. Layout is basically an layout of the entire assembly line to understand the process and the flow of work.Layout sheet will give you information about all the fixtures are placed the robots are going to work on it.
Layout Provides information of
- Flow of parts
- Station Pitch
- Robot Stations
- Accessories like Tool changer and tip dresser
- Sub assembly links
- Platform height
- Loading/Unloading Sequence/heights
Q6. What is Ergo data?
Ans. Ergonomics refers to the study of Human behaviour and Movements
Ergo data Provides information of Loading height working safety zone of operator etc
The ergo data like the height, distance from the fixture is given as an input by the customer and the design of the fixture must adhere to these data.
This design will result in ease of operation for the operator of the fixture.
Every company have standard ergo data and they provide it to fixture designer to design fixture considering that points Ex. height of fixture is decided according to ease while working on fixture. So, we have to design a fixture by considering safety, easy and fool proof design. Ergo Data is used to reduce human errors, increase productivity, human comfort, and safety.
Q7. What do you understand by Weld study?
Ans. Weld study is important information collected from the customer. The Weld study gives information about the Weld gun, Weld matrix, and weld points. The weld point is the points the weld is going to happen.
The weld points are very important data and changing those points would result in the improper assembly of the part in the Fixture. Also, it gives information about the number of geo weld spots as well as the number of Re-spot welds.
These spots will be indicated using red and green spheres respectively.
Geo Weld points are those which are welded in a geo fixture. These points are important as they make sure the assembly is not distorted while taking to a respot fixture.
The respot weld is done after the geo weld. These welds add strength to the assembly before it is being married with other panels
Q8. What are the criteria for percentage completion in the designing stage? Explain it in detail
Ans It is used in the design and dispatch stages of the welding fixture. It shows the number of tasks completed in the project and we can make sure whether the work is being done as per the planned schedule.
Different stages in a project have a different percentage as follows
Input and concept design 0-25%
Concept approval and Simulation check 25-40%
Design Freezing and detailing 40-80%
Check and Final Dispatch 80-100%
Input and concept design 0-25%
It is the initial stage of the project where we get all the design inputs from the customer and based on those inputs a design concept of the project will be created.
Concept approval and Simulation check 25-40%
Once the concept is designed it is sent to the customer for approval and the simulation checks are done for the given design and looked for the feasibility of the design.
Design Freezing and detailing 40-80%
The changes are done to the design if the results of the simulation checks force us to do or if there any changes suggested by the customer. After all these changes are done the design is fixed and the detailing to the design starts
Check and Final Dispatch 80-100%
After the detailing, it is sent for the quality inspection and finally dispatched to the customer.
Q9. Brief about "Output" in design?
Ans. The output is 3D models and 2D drawings of the tool. The output tools are of two types
Unitised tools
Non-unitized tools
Unitised Tools: The tools which are mounted in a common base like the pin unit, clamp unit, rest unit are all called unitized tools.
These tools require two types of drawing sheets namely
Key sheets and layout sheet
Key Sheet: Key sheet mentioned or shows the location of every units in fixture.
Layout Sheet: Layout sheet is detail drawing of particular unit in fixture.
Non-unitised Tools: This type of tools don't require key sheet. Ex. stands and tool changer. Tools that can stand alone and details in layout sheet. Non unitised tools are stand-alone tools like gluing stand etc
They need only a layout sheet and can be detailed solely on it.
Q10. What do you understand by structuring a design tree? How does it reduce errors during the design process?
Ans. Structuring a design tree is very necessary while designing fixture because it help to identify all manufactured part in whole fixture. Every customer company have their own standard. This will help us during design study, manufacturing, and inspection to avoid errors.
Structuring a design tree implies a process where all the assemblies and parts are named in a specific standard. Every customer will have their own set of standards to structure the design tree. It is an important process that helps us to identify the specific part or assembly as to which project, tool/unit it belongs to.
This helps us to avoid errors during design study, manufacturing, assembly, inspection. If the parts are the assemblies are not named properly or the design tree is not structured properly, it will create confusion to understand the design and may create major possibilities of making an error.
The naming of a fixture or a unit or a part gives the information as to which project, tool or unit, it belongs to It can help us identify the number of items of the same type or different type that are being used in an assembly. Two or more components which have similar design are given the same name such that one component is taken as a reference during manufacturing.
Q11. What are Units? Mention 5 types of units
Ans. Units is a device that has a specified function, especially one forming part of a complex mechanism. The fixture is the assembly of different units. Some of the units used in fixture assembly are the Base unit, Pin unit, Clamp unit, etc.
Some of the units are:
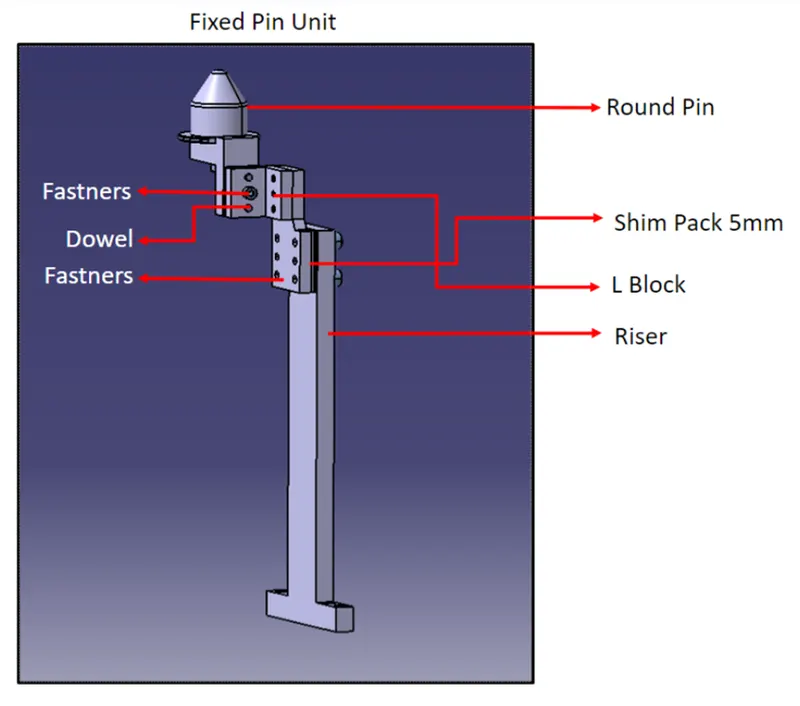
- Fixed Pin Unit: Fixed Pin Unit is non movable locating unit which arrest movement of component in fixture.
- Retract Pin Unit: Retract Pin Unit having retracting unit which is used to move pin to ensure proper loading and unloading of component.
- Rough Locator Unit: This unit help operator for correct loading of component.
- Rest Unit: As name suggest, rest unit is used to rest the component.
- Base Unit: All the units in fixture are placed on this base unit.
Q12. Describe fixed unit and its parts.
Ans. Fixed pin units are used in a fixture to locate the car panel during any operation.
Pin, Pin retainer, Shims, blade, riser are the parts of the fixed pin unit.
Pin retainer is used to mount the pin.
The pin retainer block has two-way shims. Shims are very important in designing a pin unit as it helps to avoid the stack up tolerances during the assembly process.
The purpose of the Fixed pin unit.
The fixed pin unit is used to arrest the 6 degrees of freedom of the assembly of a fixture. The other six degrees of freedom are arrested by the three rest units.
Pins help to locate the part of an assembly very accurately for the welding operation.
Q13.What are the different parts of a fixed unit?
Ans. The different parts of a fixed pin unit are as follows
- Pin: Pins are used for accurately locating the part to welded in an assembly.
- Pin Retainer: Pin retainer is used to hold the locating pins.
- Shims: Shims are small parts of the thickness of 0.1,0.2,0.3 mm. The shims are used to compensate for the difference due to the stack-up tolerance of the assembly, which eventually results in the improper holding of the panel if the Mylar holds it loosely.
- Blades: Blades are plates that are attached to the raiser.
The cylinders and other additional arms are mounted on a Blade.
- Riser: A raiser is a part that is used to raise the height of the fixture.
The raiser is fixed to the base of the fixture and the blade is mounted on the raiser
Q.14. What is the purpose of making a rest unit & describe its parts ?
ANS. Rest Unit is one of the simplest unit in fixture used with myler. As rest unit is simple to manufacture and require low cost, hence rest unit is combine with clamp unit and location unit. Rest unit consist of following parts:
RISER: Riser are used to increase height of unit and these are standard parts so need not detailed it or designed it.
BLADE: As shown in figure blades are bolted on riser.
SHIMS OR SPACER: Shims or spacer are used to compensate tolerance stack up. In pin unit we need to control two direction that are X and Y using shims or space. Shims are generally thin sized plates used in group called Shimpack and spacer are used as single plate and can be machined accordingly. single-plate - solid standard shims for vertical alignment
MYLARS: Mylars are the parts in the rest unit which are in contact with car panel or component used to give support or rest to the component.
Q15.What are the basic fundamentals to design a Sensor unit?
Ans. A sensor unit is used to sense whether the car panel is placed in the fixture or not.
The sensors will send the signals to PLC systems and so the next process will be executed by this signal.
The number of sensors used in a fixture will depend upon the number of parts used for the assembly.
Every panel should by one or two panels depending on the size of the part and in such case they are placed in the opposite direction.
The mounting of the sensors should be in such a way that they are adjustable in three directions.
Some of the major sensor manufacturers are IFM, SICK, OMRON, etc.
Q16. What is a rough locator unit & what are the basic fundamentals to consider while designing it?
Ans. Rough locators are majorly used in manual fixtures.
The rough locators will guide the operators to place the part in the correct position and orientation.
The rough locator can be a standard part or make part.
The fundamentals of rough locators are as follows
- Rough locators have to be placed at the edge of the car panel in order to guide them.
- There must a gap of 2-5 mm between the rough locator and the car panel in order to avoid damage during loading and unloading.
- Rough locators have to be placed at the same angle as the car panel.
- Rough locators should guide the panel in pin arresting direction.
- Rough locators should start guiding the panels 10-15mm before the pin engagement
- Rough locators should be designed with an entry angle for the car panel which is around 35-40 degrees.
- Rough locators should be designed with two slots to mount for easy adjustments.
- The slots should be in direction of the car part guiding.
Q17. What is a Base unit and describe its parts?
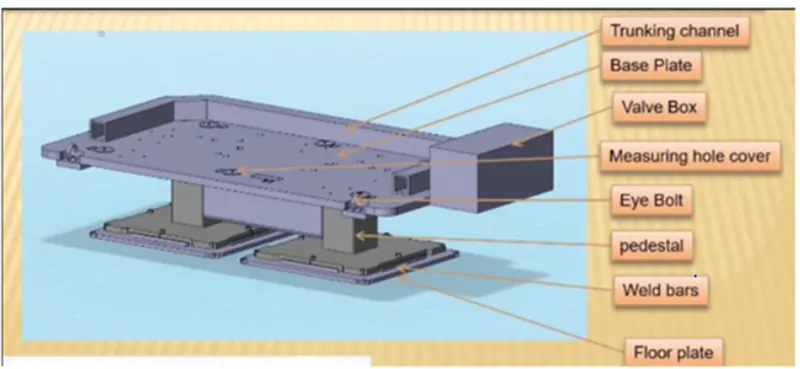
Ans. The base unit is designed to mount all the other units like clamp unit, pin unit, rest unit, etc of the tool, also other parts like pneumatic valve box, trunking cable path will also be mounted on the base unit.
The parts of the base unit are as follows:
Valve box
Trunking Channel
Measuring hole cover
Eyebolt
Pedestal
Floorplates
Valve box: A valve box is used to supply pneumatic cylinders assembled in the fixture.
The valve box consists of solenoid valves with an inlet and outlet which controls the supply of air to the cylinder.
Trunking channel: Trunking channel is a hollow passage that guides and covers the pneumatic and electrical linings.
Measuring hole cover: The measuring hole cover the coordinates of the measuring holes are mentioned. These coordinates are used as references for placing the other units and also for the CMM inspection purposes.
Eyebolts: Eyebolts are placed in the base unit in order to lift the base unit and move it from one place to another.
Pedestal: The pedestal is a stand-like structure where the entire unit of the base will be mounted.
Floorplates: Floorplates are used to mount the entire base on the floor.
Q18. What is a Dump Unit and what are its function ?
ANS. Dump unit is used due to lack of space on fixture to build a unit. So, this is a complex unit consist of dump cylinder used for clamping or unclamping of car panel or component. Dump unit is found in complex fixture. A dump unit is used when there are geometrical constraints while placing a panel. It consists of a dump cylinder to perform clamping and unclamping operation.
FUNCTION:
Due to space constrain dump unit used in fixture. It has dump cylinder having open and close position for better understanding of design. It also has clamp cylinder used for clamping purpose.Hence this is too complex unit to built.
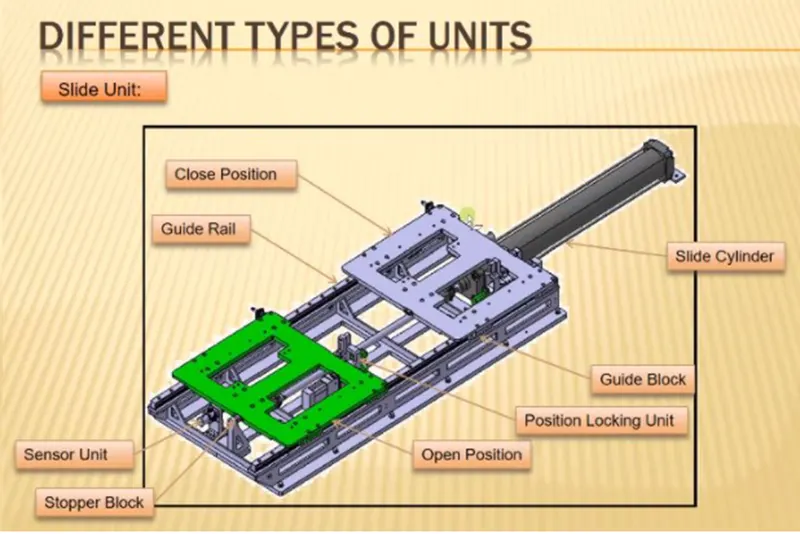
- What is a Slide unit? Mention where Slide units are commonly used
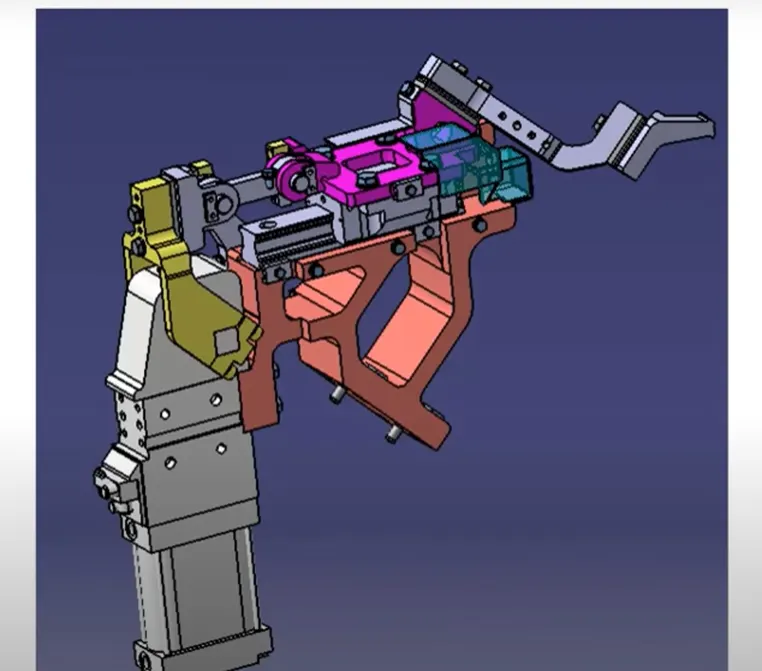
Ans. Sliding units are used in a fixture when there are a lot of space constraints, where usage of different units is very difficult in order to design the assembly.
The sliding unit consists of a sliding cylinder to which a panel is attached
The panel moves on the guide rails provided and this motion is due to the reciprocating motion of the cylinder
The position locking units are used to lock the position of the panels on the guide rails
Sensor units are used to detect the position of the sliding plate, whether it has reached the desired position or not.
A stopper block is used to control the motion of the sliding plate.