Week 12- Final project
AIM: To design the car door inner panel with reference to given Class-A surface by using given master-section, creating attachment features and performing draft analysis to check the manufacturing feasibility of the component by using software CATIA V5.
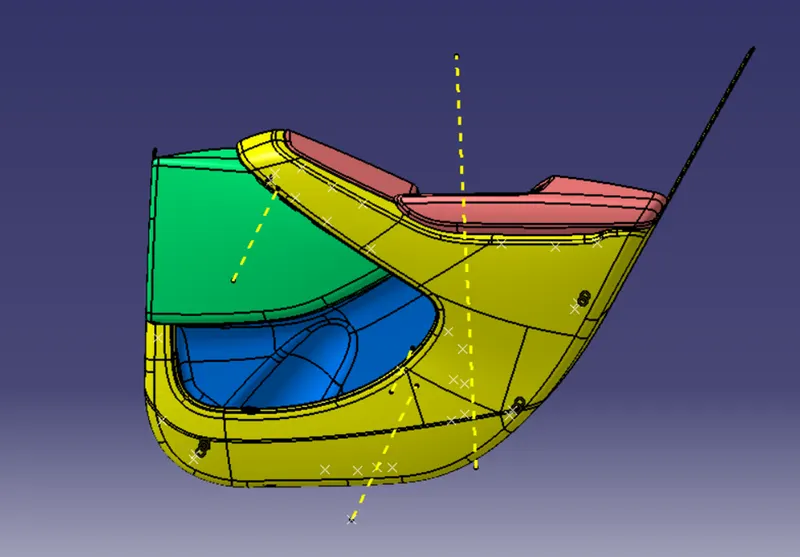
Objective: The project deals with the explanation of method followed to develop door trim inner panel. In this with the given Class-A surface, Class-B surface and Class-C surface were created along with the tooling axis. Other attachment features were also created for assembly of the different components of door trim.
Methodology:
The methodology of the project is explained here:
1. Class-A surface was extracted from the given surface.
2. Tooling Axis were created of the individual component.
3. Class-B and Class-C surface were created with the OEM guidelines.
4. Formed Solid body from the closed surface.
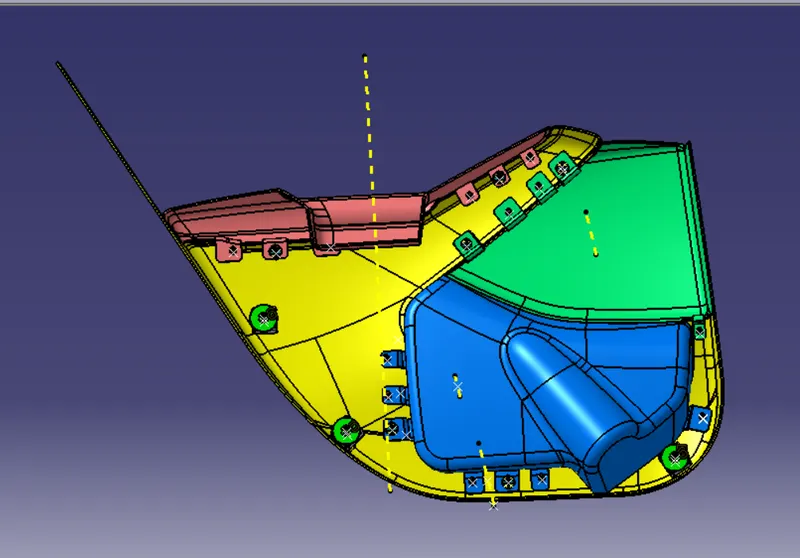
5. Engineering features were created for attachment.
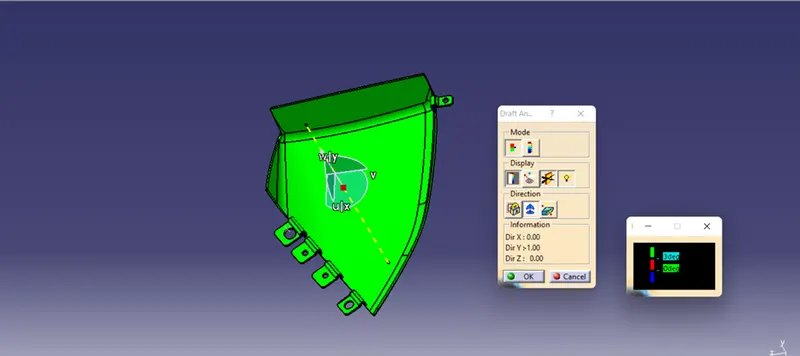
6. Draft analyses of each component were performed to check the manufacturing feasibility.
Introduction:
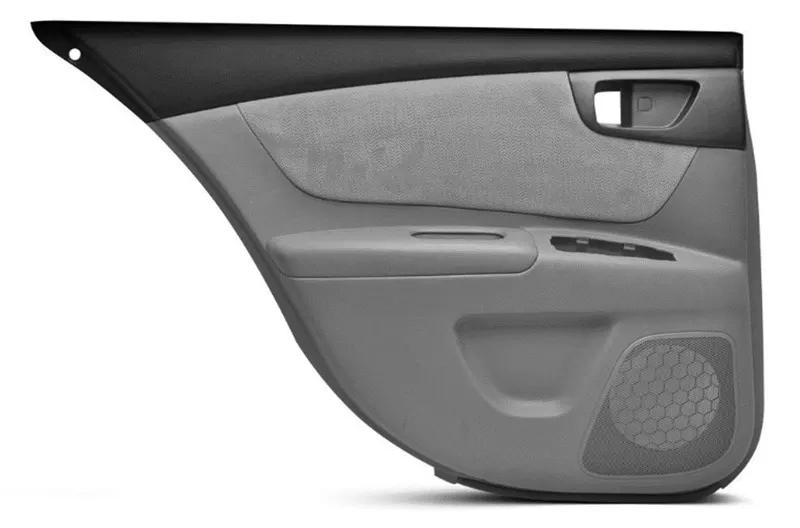
The inner door panel is an aesthetic and functional component in a car, it is the interface between the car interior and the inner working of door. Inner door panel usually consists of armrest, map pocket, bottle holder, handle bar, other switches, upper and lower substrate, storage compartments, convenience (puddle) lights and locking mechanism. Nowadays door panel is made of plastic material like polypropylene, ABS etc. which helps in making lightweight and complicated shapes of door panels.
The manufacturing Process of plastic door panel is called Injection moulding. In this manufacturing process the heated molten plastic material is injected into the mould between core and cavity and cooled down to form a solid plastic component.
PROCEDURE
Given CLASS-A surface with Master-section
Components included in door panel
- Map pocket
- Bottle holder
- Lower substrate
- Armrest
- MAP POCKET
CLASS A SURFACE
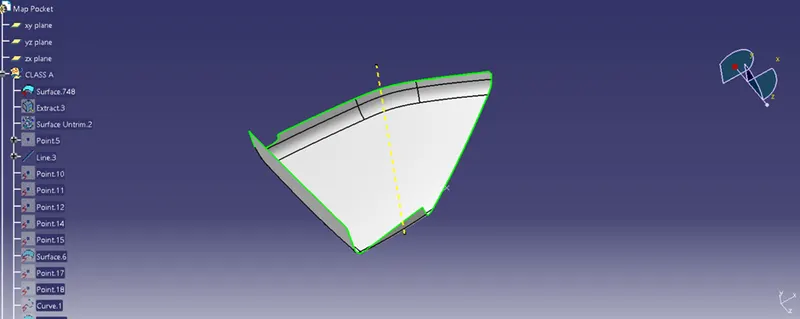
CLOSED PART BODY OF MAP POCKET WITH FLANGES
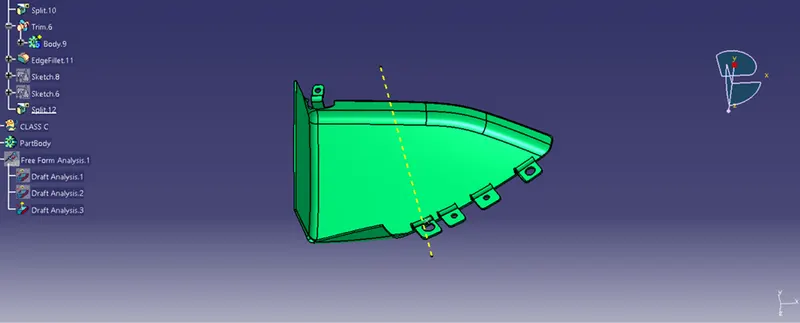
DRAFT ANALYSIS
2. BOTTLE HOLDER
CLASS A OF BOTTLE HOLDER
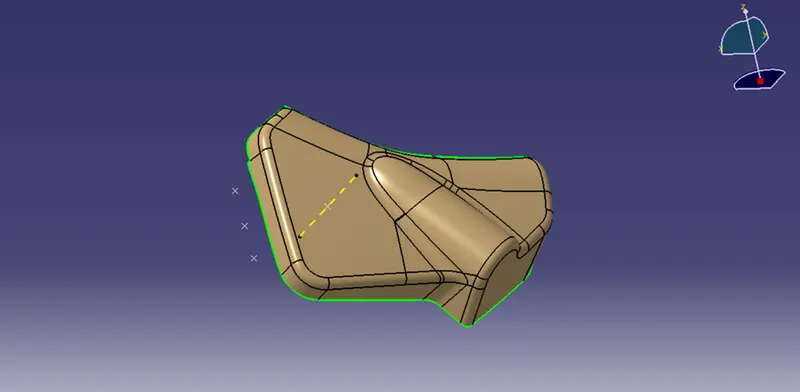
CLOSED BODY
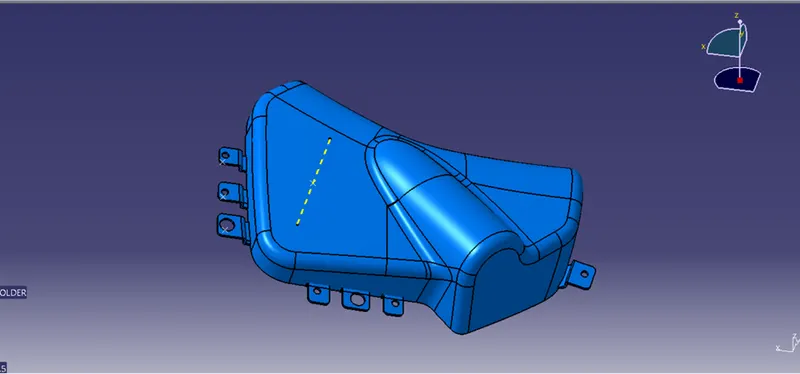
DRAFT ANALYSIS
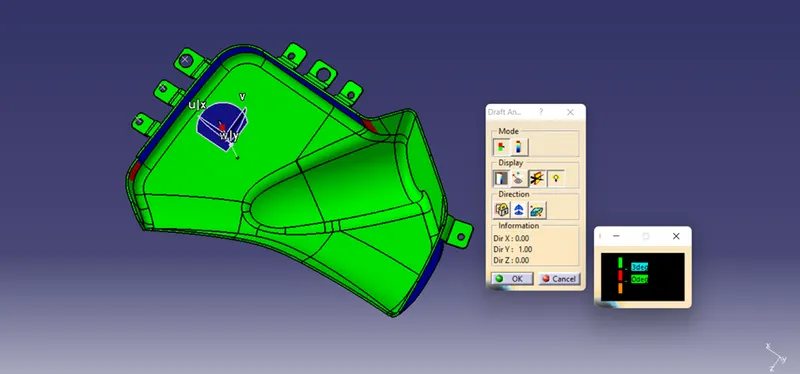
3. ARM REST
CLASS A SURFACE
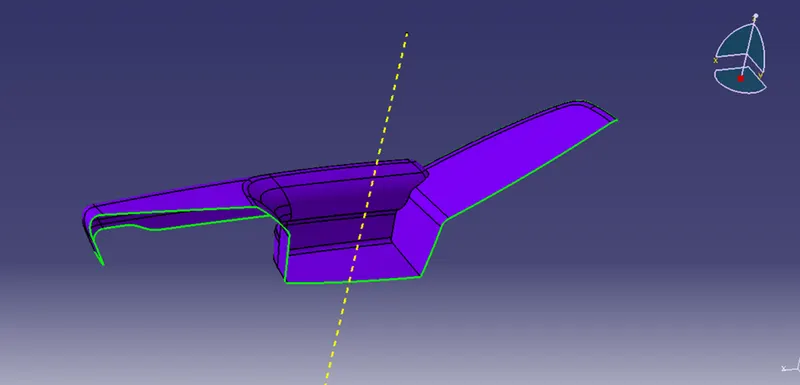
CLOSED BODY
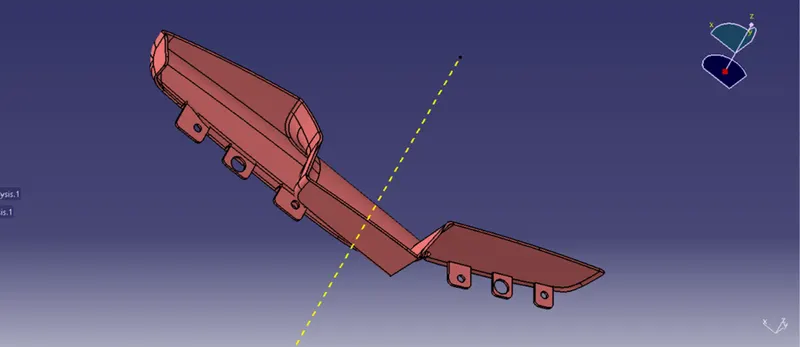
DRAFT ANALYSIS
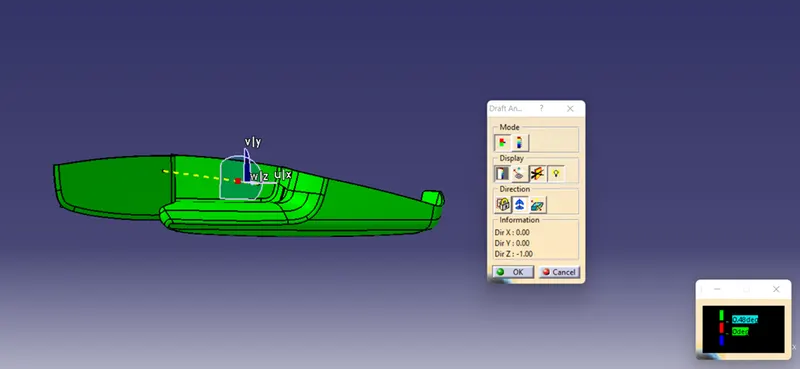
4. LOWER SUBSTRATE
CLASS A SURFACE
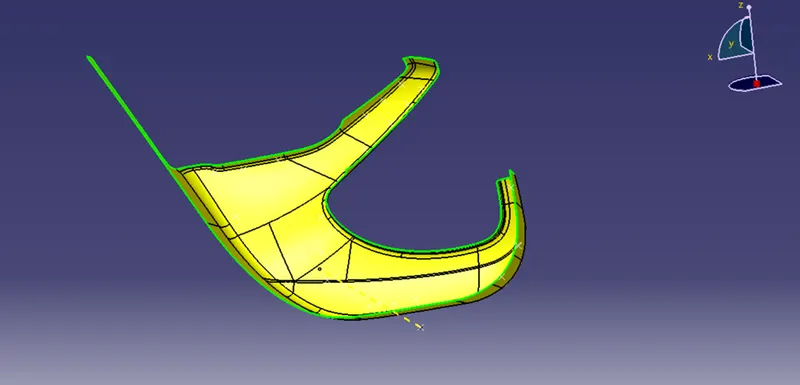
SOLID BODY
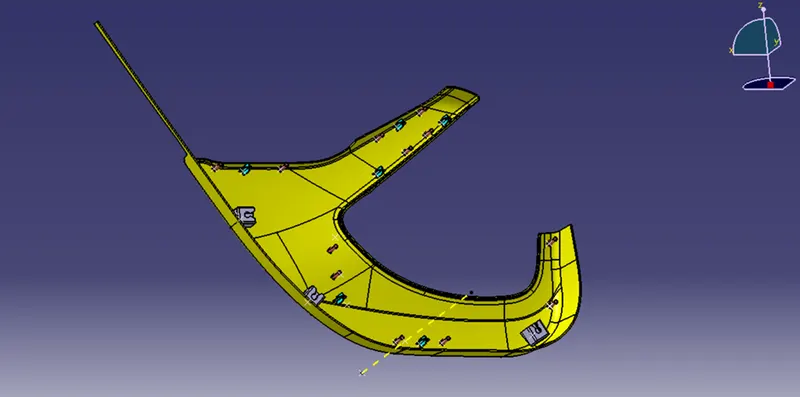
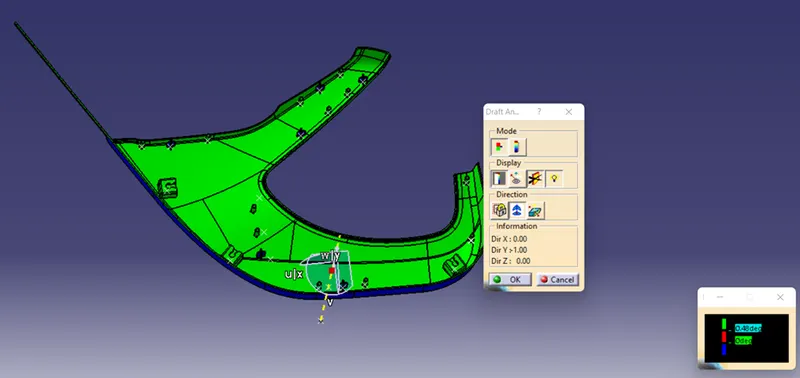
DRAFT ANALYSIS
Attachment features
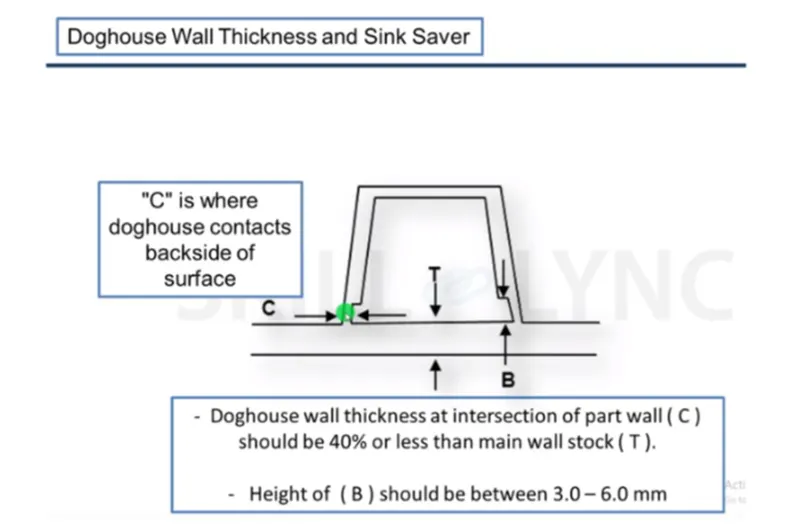
DOG HOUSE- Doghouse is an engineering feature used in the plastic trim design which helps to remove sink marks formed on Class-A surface while creating attachment feature on Class-B surface. Doghouse is a supporting feature, other features like locators, heat stakes, pushpins are mounted on top of doghouse for fixing and assembly purpose. Doghouses are subjected to draft analysis to prevent breakage of the component during ejection from the mould.
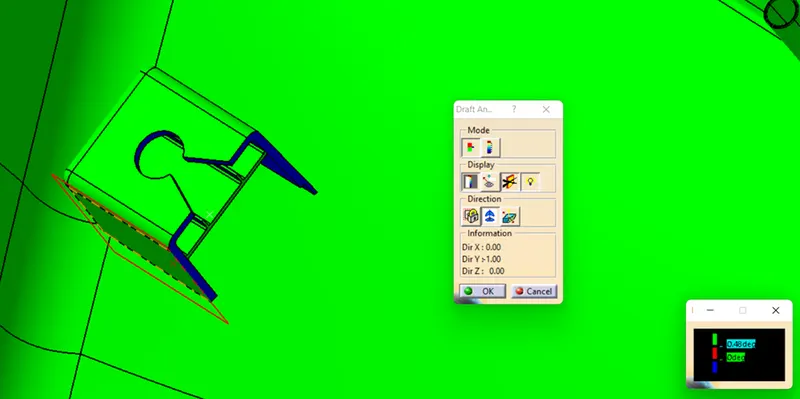
Flanges- Flanges are the joining features that help to assemble different components. The master section was used to make flanges. After creating one flange axis to axis system was used to translate the flanges. The draft of 0.5 is given to the flanges. The gap between flanges should be 60-100 mm. Boolean operations were used to add attachment features into closed body.
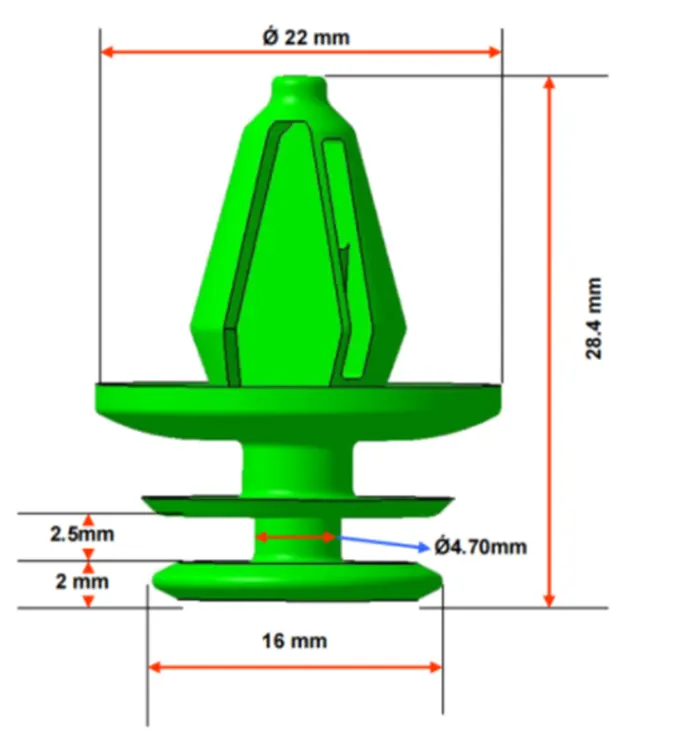
PUSH PINS- Push pins are used for joining one component to another. These are basically attached to the doghouse. For creating the push pins the following reference was taken for dimensions.
HEAT STAKES- Heat stakes also known as thermoplastic staking; it is process of joining two dissimilar materials together. In heat staking, local heating and cooling is used to raise the temperature of plastic components and allow plastic reforming to be carried out. This reforming can be used in a wide variety of applications.
Applications range from staking plastic bosses for assembly of car door panels to joining PCBs to plastic housings. Benefits of his technique includes; no vibration damage, no particulates, the ability to stake metalized coated application and the capability to stake in difficult to access or restricted areas.
The progressive melting of plastic under continuous pressure forms the head. When staking the right combinations of heat and pressure for the applications is critical.
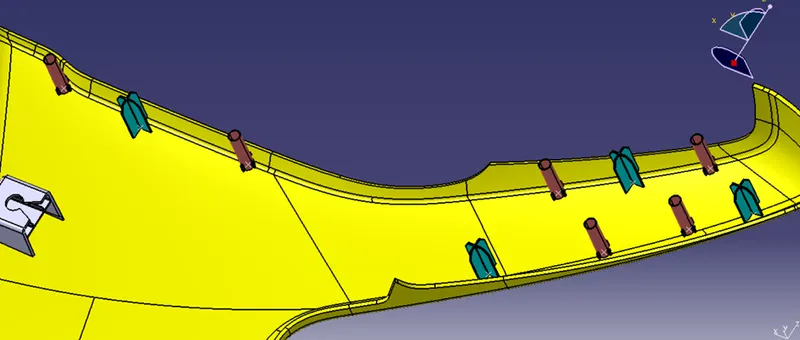
The advantages of heat staking are as follows:
- Simplifications of the machinery
- Reduced cost of machinery.
- Multiple fastening point.
- Allows higher density of welds compared to hot air, cold form or ultrasonic welding.
Ribs- Ribs are the feature that provides stiffness to the parts and toughness without increasing the thickness of the part.
Locators- Locators provide easy alignment to the parts which are mating with each other.
The design rules of ribs
- Rib thickness should be 0.4 times of thickness of the part.
- The walls of rib should be drafted with 0.5 degrees draft.
- Top height of ribs should be at least 5 times part thickness
- Thickness of rib at tip should be equal or less than 0.75mm.
- Maximum fillet vale should be 0.25mm Radius.