Week 11 - Final project
AIM:-
To create a solid body of Side Door plastic trim including the engineering features using CATIA V5 tool using the given Class A surface and master section and adding thickness to the component.
INTRODUCTION:-
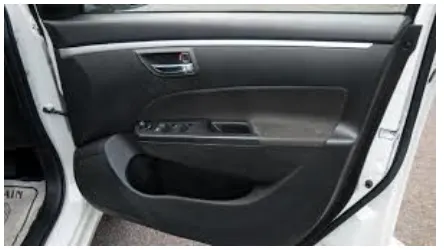
Side Door Plastic Trim
An interior plastic component attached to the inner side of the door. This product improves the appearance of the vehicle intertior and also creates a more comfortable interior by providing a variety of fitments and functions.
OVERVIEW OF DESIGN LIFE CYCLE IN AUTOMOTIVE INDUSTRY
Product Development process
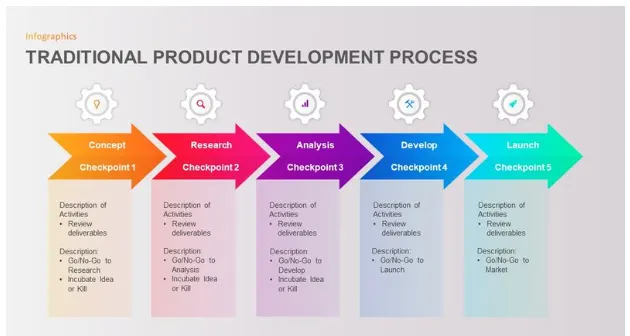
- Concept/ideation
This is the concept and ideation stage during which a product's functional and performance requirements can be defined along with buyer's ideation. customer requirement and innovative design ideas are explored freely to find the sloutions to the present market need.
- Feasibility study and design planning
The feasibility phase gives the management an opportunity to evaluate a project's potential, reviewing the project from various business angles. During this phase, the project team reviews product design concepts. Then they select the design that best suits the user requirements.
- Design and development
In this phase formal engineering specifications are created. Verification and validation plans are developed for the future instances. These are the final quality checks that will systematically determine that all the agreed specifications are present and working in the end product. Then the product is then developed gaints the designs, with regular checks made throughout the process to access and lower the risk of its failure for the end user and the project itself.
- Testing and verification
Comprehensive testing of the final product takes place to evaluate the robustness of the design and its ability to meet the customer requirements. Verification takes place against the design requirements identified in stage 2.
- Manufacture/launch
Plans, specifications and other relevant documents are transferred to the manufacturer for production, or software products and updates are released to the customers. Marketing and launch plans are finalised and activated.
- Improvement
The new product becomes part of the company's portfolio. ongoing product management ensures the product is subject to continuos upgrades and improvement.
The stages of Design life cycle are
Concept Sketches:
Concept sketches are rough ideas of free hand sketch obtained through styling team and will be used to prepare the model. It is usually done through pen and paper and through painting software. This will be used to generate the concept for preparing the model by incorporating various styles and information obtained through stakeholders.
Class A creation:
After finalizing the concept, the sketches are usually worked in software's such as AutoDesk Alias to create Class A surface.
Clay Modeling:
The Class A Surface is concurrently worked by the clay modelers to brainstrom abd benchmark the styling of the product and later the concept is validated by bringing up a rough clay model and then it is passed on to the design team for the preparation of New Product Design(NPD) CAD.
NPD CAD:
This is where the development of surfaces to parts in CAD kick off and design engineers involvement is vital in this stage.
The designers will work on the input Class A surafces which are validated from the feasibilty team
The procedure followed in creation of the plastic New Product Design are
- Tooling axis
- B Surface Creation
- C Suraface Creation
- Closed Body Creation
- Draft Analysis
PROCEDURE OF PART CREATION:
1) Input Given:
Design of Interior Door Trim:
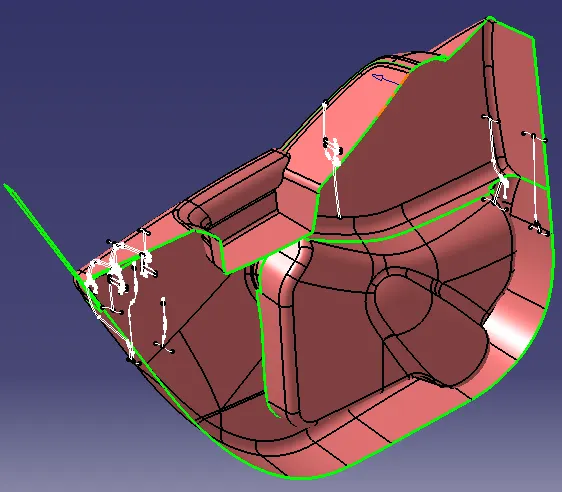
Interior door trim consists of four components
1) Lower Substrate
2) Upper Substrate
3) Map Pocket
4) Door Arm Rest
2) Class A Surface:
In Automotive design, a Class A Surface in any of a set of freeform surfaces of high efficiency and quality. Although, strictly, its nothing kore than saying the surfaces have curvature and tangency alignment- to ideal aesthetical reflection quality, many people interpret Class A surfaces to have G2 or even G3 curvature continuity to one another. Class A Surfacing is done using computer aided industrial design applications. Class A surface modellers are also called "digital sculptors" in the industry. Industrial Designers Develope their design styling through A-Surface, the physical surface the end user can feel, see, touch etc.
Door Arm Rest
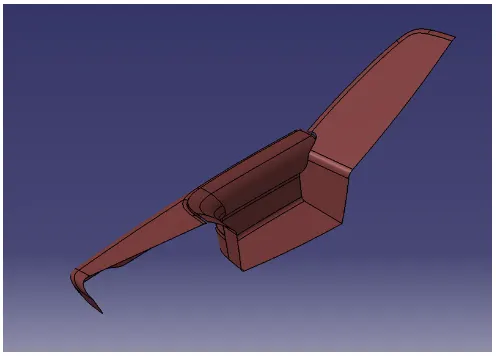
Map Pocket
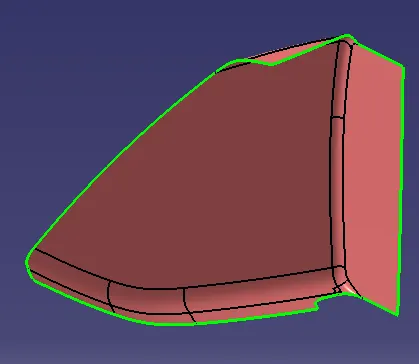
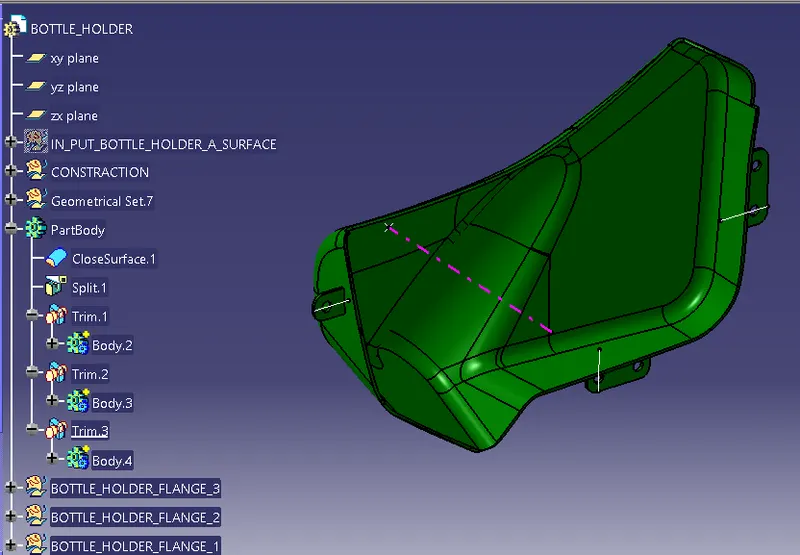
Bottle holder
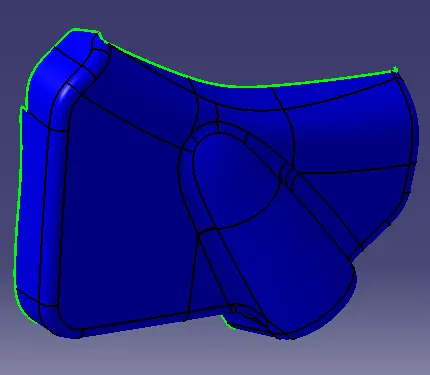
Lower Substrate
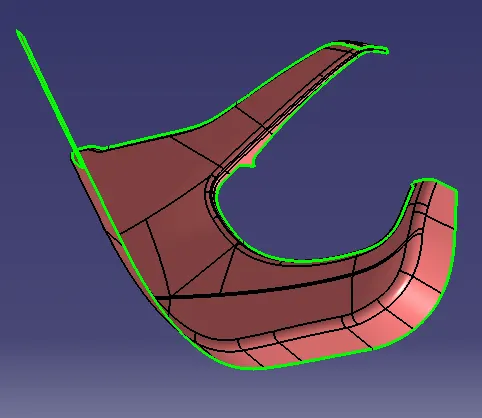
3) Tooling Axis:
Tooling axis is nothing but the direction in which the core and cavity opens and closes. Design engineer works on it to analyse the Class A surface and finds out the best possible tooling direction keeping in mind all the draft angle is with respect to the tooling axis so that the component can be easily ejected from the moulds.
Door Arm Rest
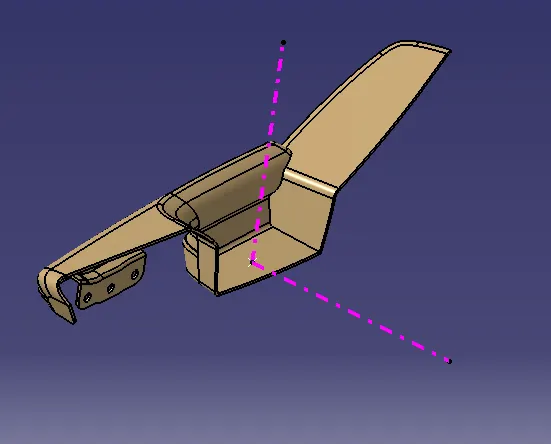
Map Pocket
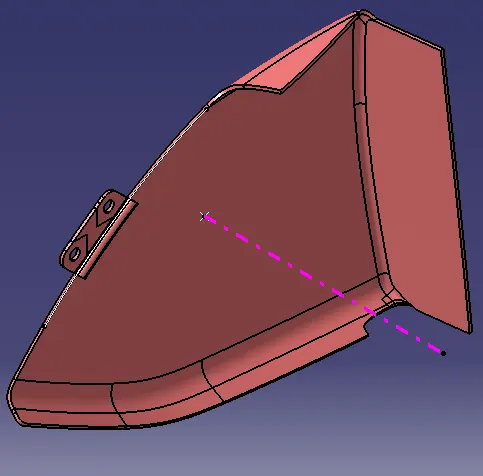
Bottle holder
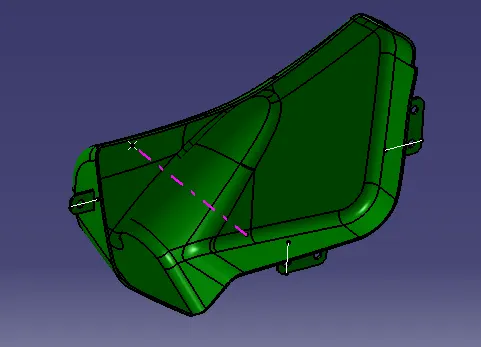
Lower Substrate
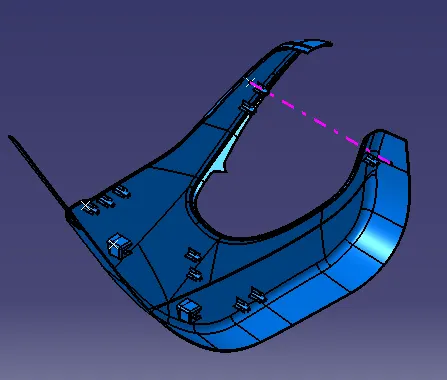
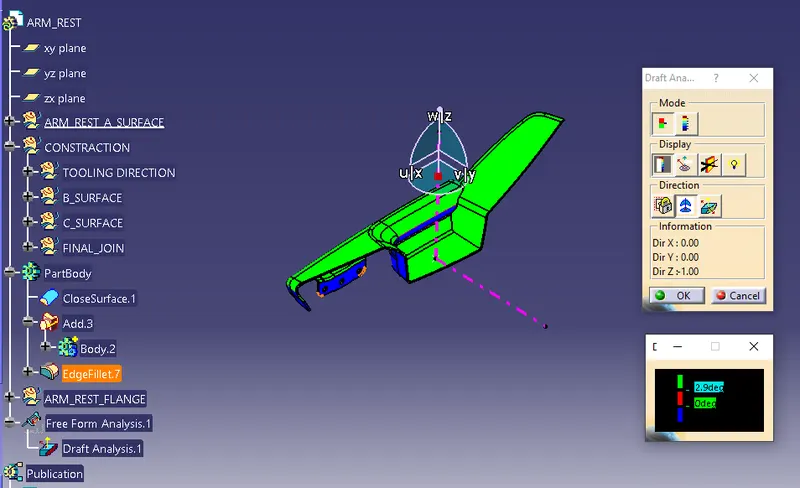
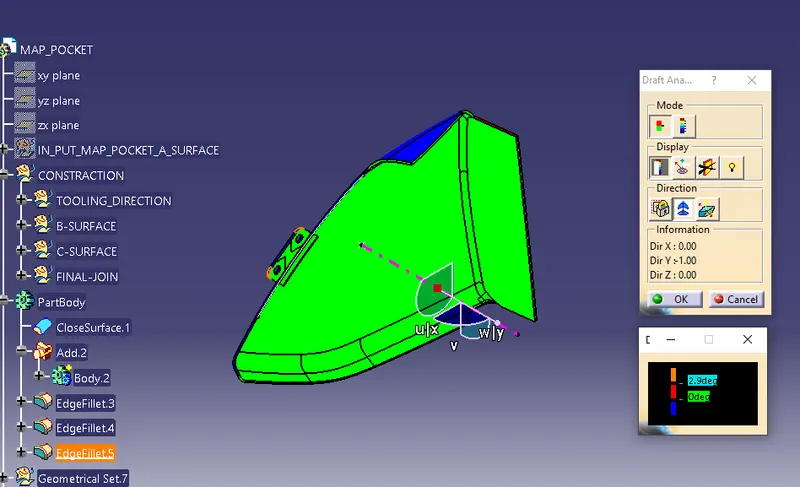
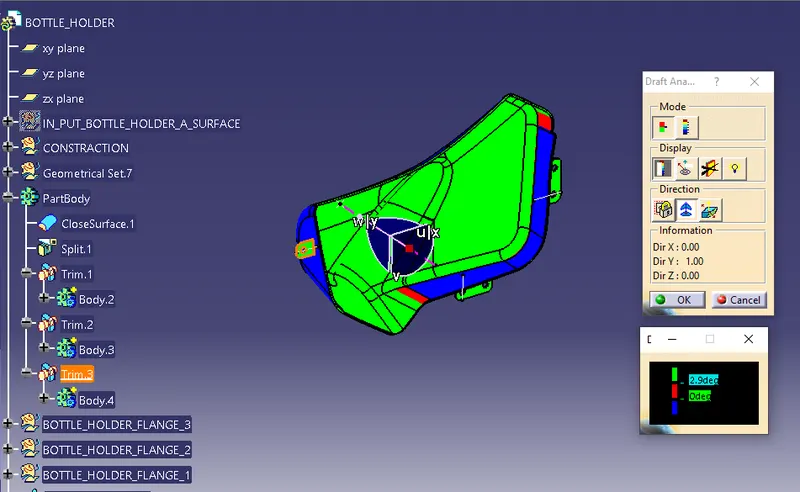
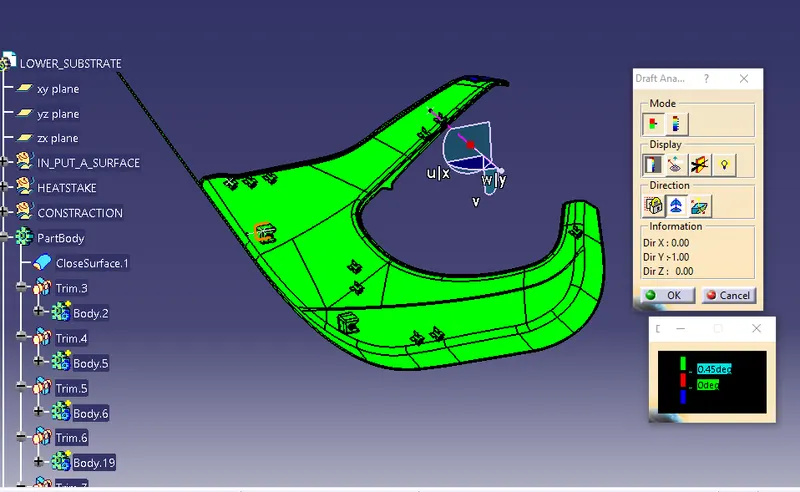
4) Draft Analysis:
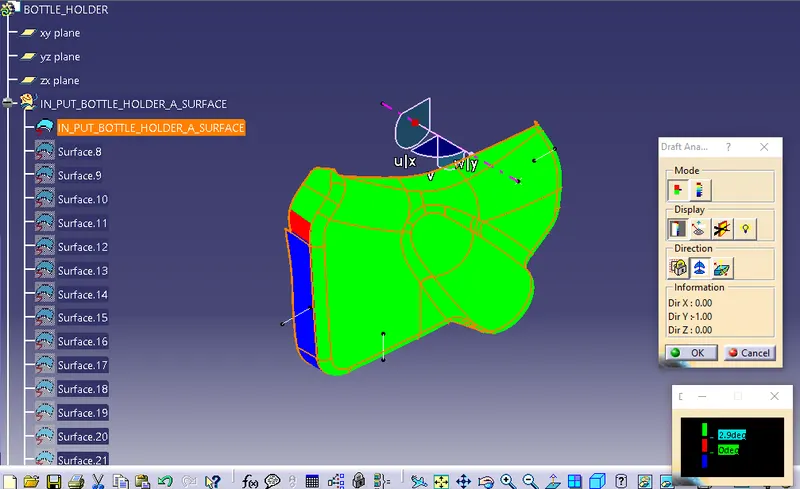
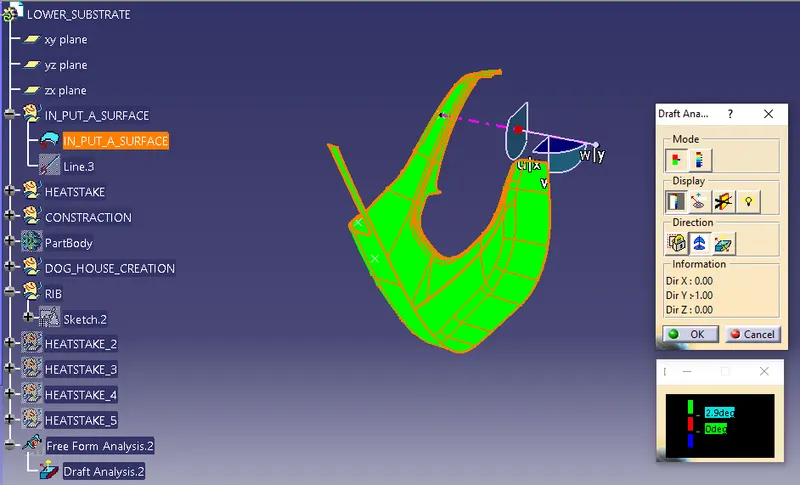
The Draft analysis command enables you to detect if the part you drafted willbe easily removed. This type of analysis is based on color ranges identifying zones on the analysed element where the deviation from the draft diection at any point, corresponds to specified values.
Draft anlges are very important in thermoforming product designs. If the product is formed onto a female or negative mould, it shrinks away from the mould side wals. As a result, true female or negative products can be thermoformed with vertical walls having zero draft angles. Parts cannot be ejected from the tool if it is at 90 degree surface. For that reason, a small draft angle is to be provided for each and every surface of the component in order to easy removal of the component from the moulds without any defects. Most of the part require minimum 0.5 degree to 1 degree, however 3 degree is widely accepted in plastic component design. Draft analysis is the technique used to analyse weather our designed product are manufacturable with required conditions are not.
Door Arm Rest
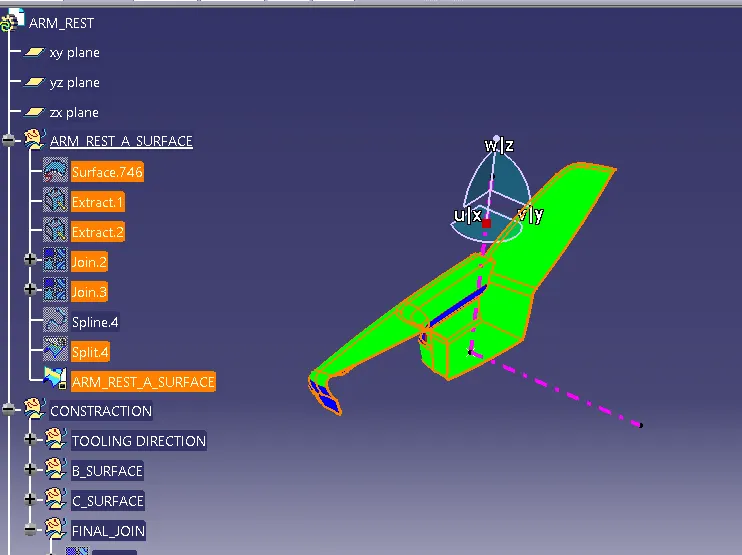
Bottle holder
Lower Substrate
5) Class B Surface Creation;
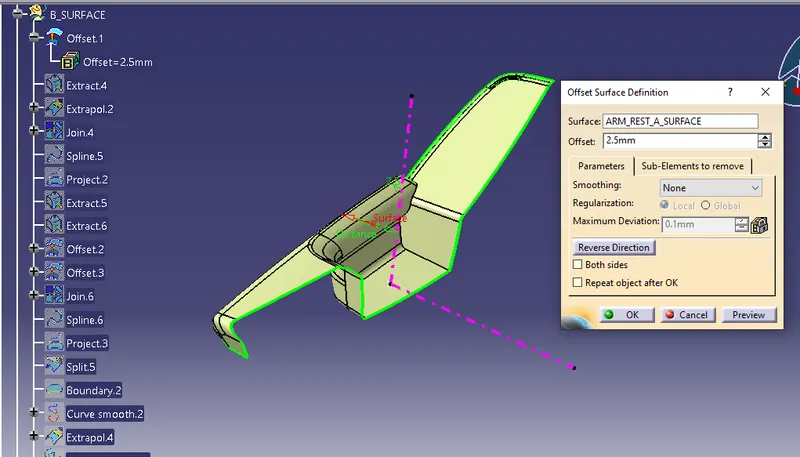
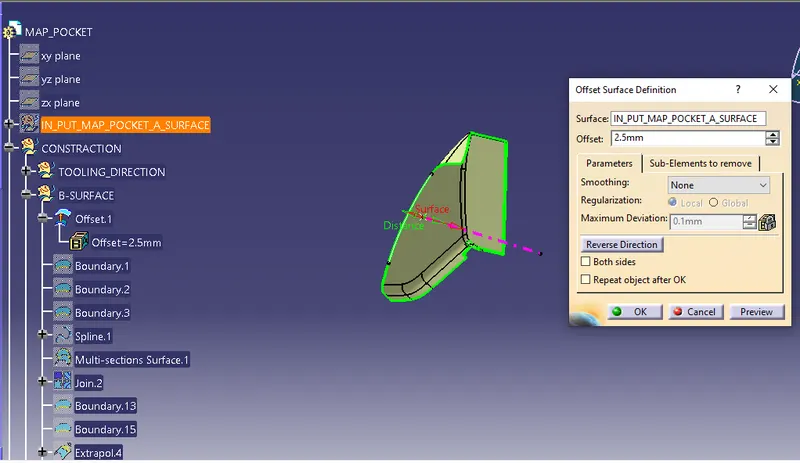
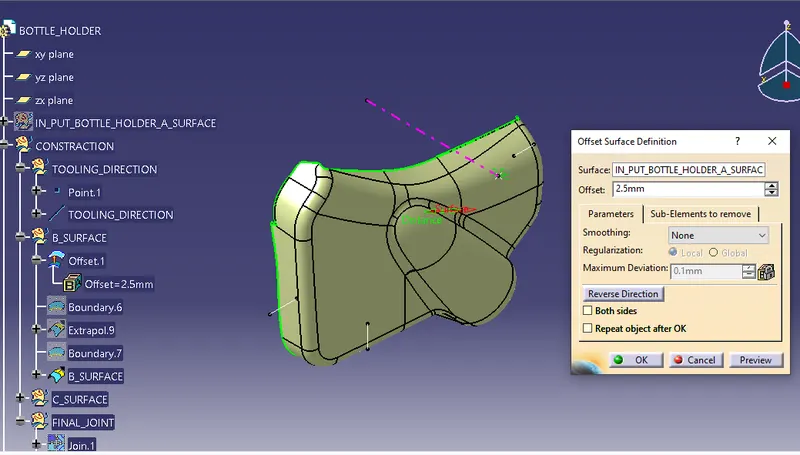
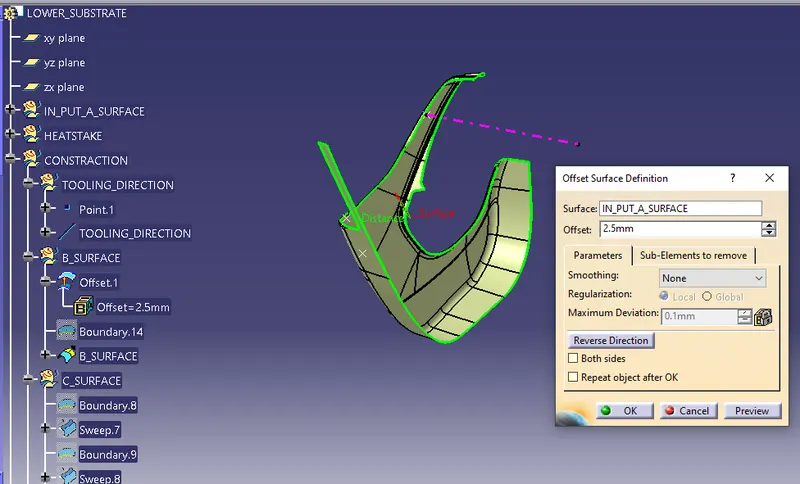
Class B surface includes derived surfaces created by offset operations from Class A surfaces to define the thickness Of the material. In this file it is important to link Class B Surfaces geometrically to enable an adaptation to Class A surfaces Automatically in case of styling change.
After creating the tooling axis, B surface is to be created which is nothing but the surface parallel to the A surface. B surface contains all the fillets and the edges which the A surface contains.
Door Arm Rest
Map Pocket
Bottle holder
Lower Substrate
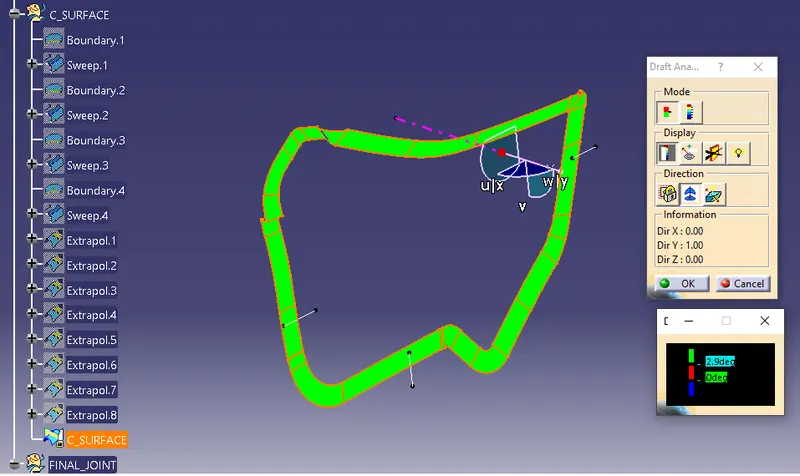
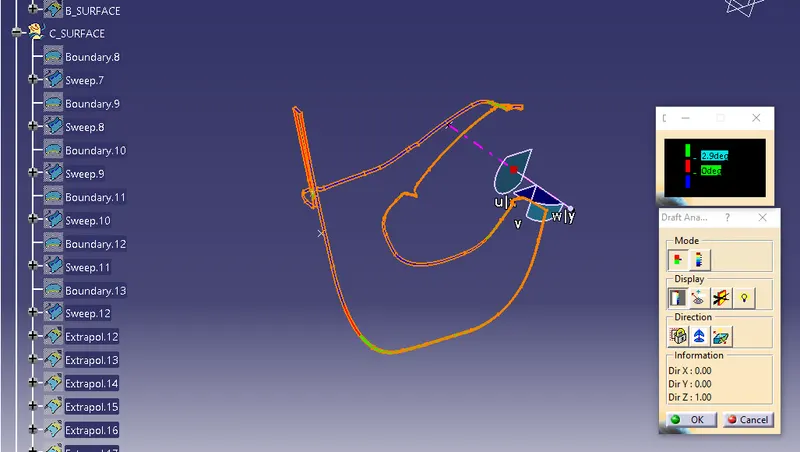
6) Class C Surface Creation:
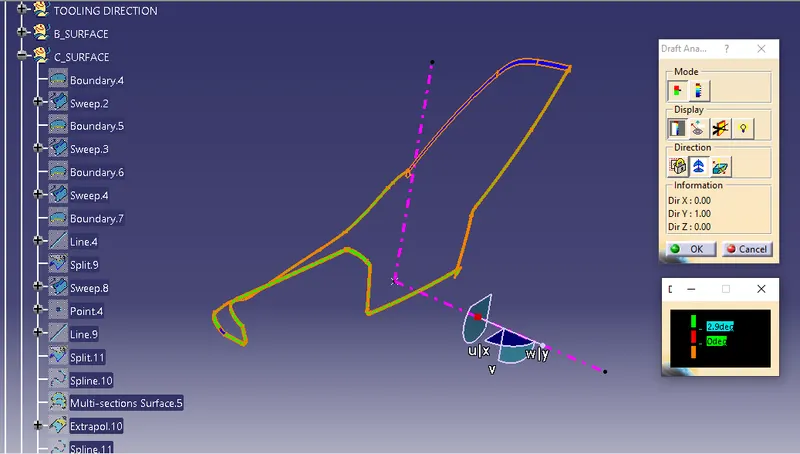
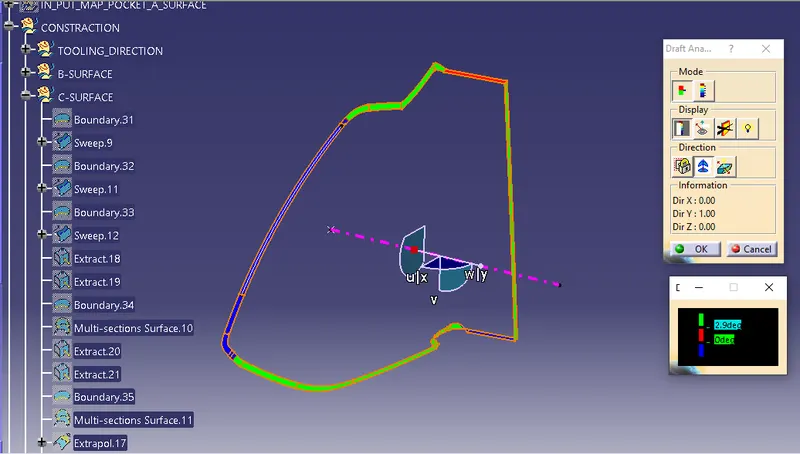
Class c Surface is swept along the boundary of the Class A at an angle perpendicular to the Class A Surface
with respect to the tooling axis direction with a draft angle of 3 degree.
Door Arm Rest
Map Pocket
Bottle holder
Lower Substrate
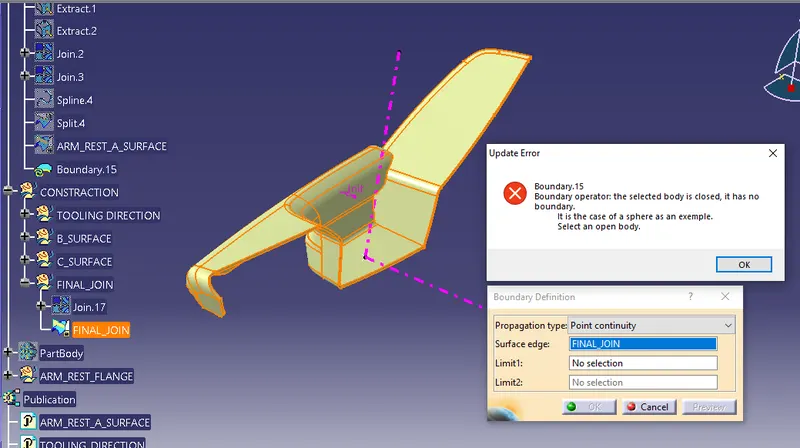
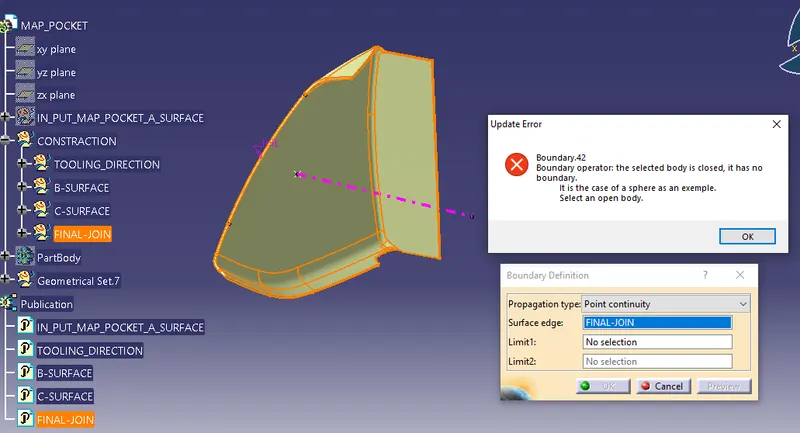
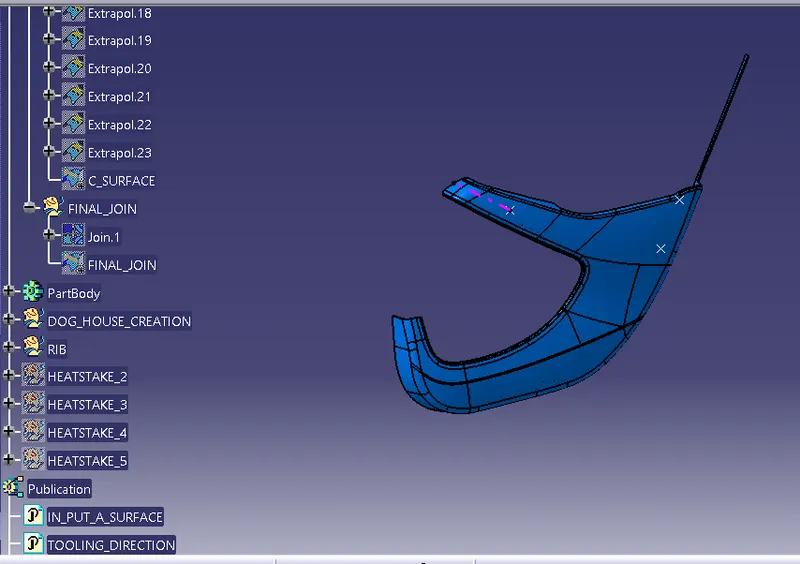
7) Joining Class A,B and C Surfaces to get a Closed Surface:
After finishing all the 3 Surfaces, join the Class A and Class C surface together using Join command. Now, the joined surfaces are then trimmed with the Class B surface to form a Closed Surface.
Door Arm Rest
Map Pocket
Bottle holder
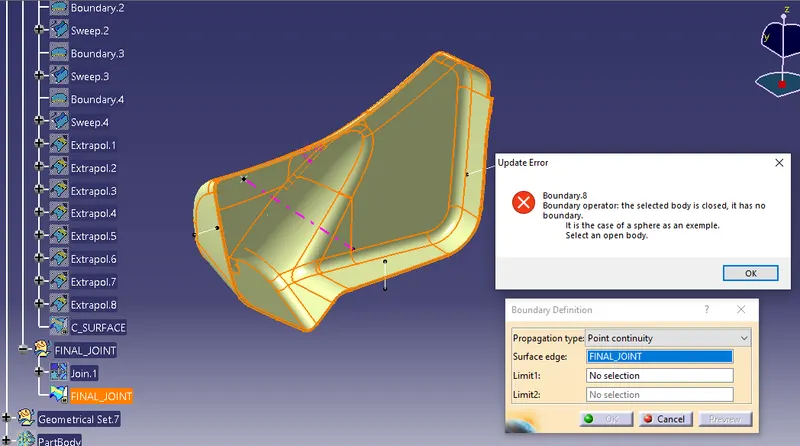
Lower Substrate
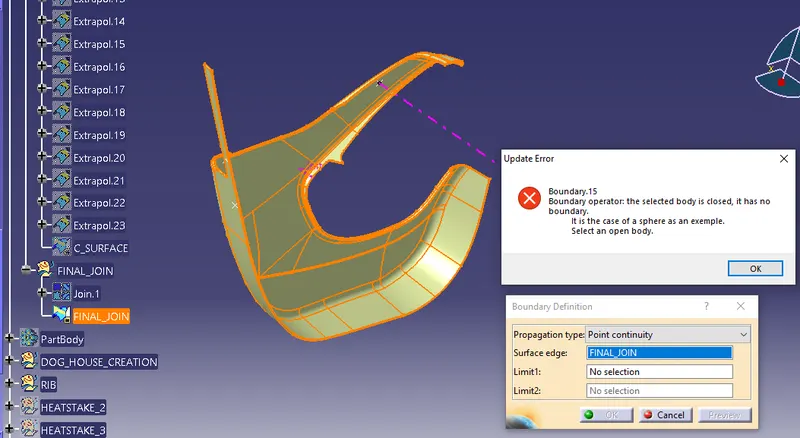
Now, Switch to Part Design and Add the Thicknessto the closed surface in order to get the closed solid body as shown in the fig below.
Door Arm Rest
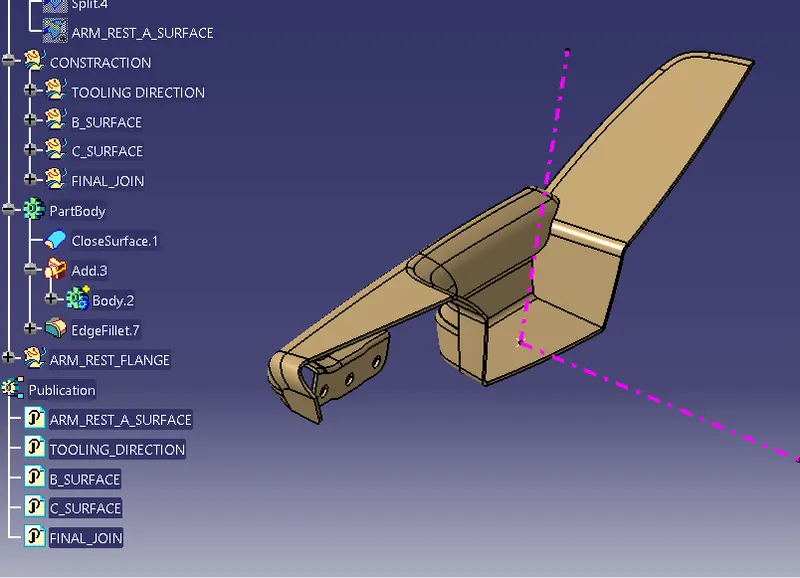
Map Pocket
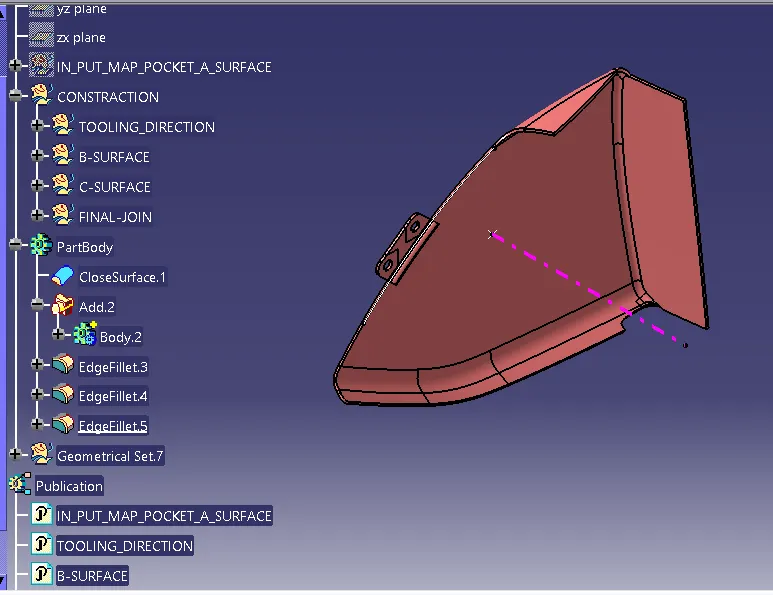
Bottle holder
Lower Substrate
8) CREATING ENGINEERING FEATIRES(Doghouse,pushpin,heatstakes)
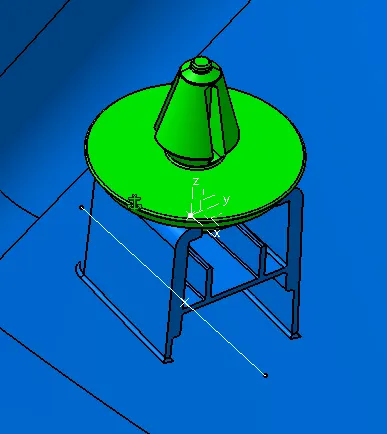
DOG HOUSE : Dog house is an engineering feature used in plastic trim design. Dog houses are used as supporting feature. Sometimes other engineering features like snaps; locators etc. are mounded on them to increase their strength.
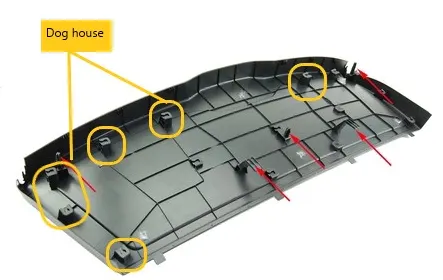
Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on B-surface.now we will proceed with creating a dog house and mount the boss on it by following the design rules mentioned below.
Doghouse design guidelines (used as reference) :
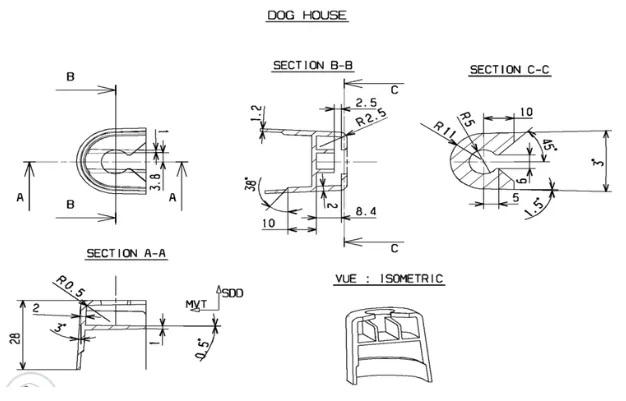
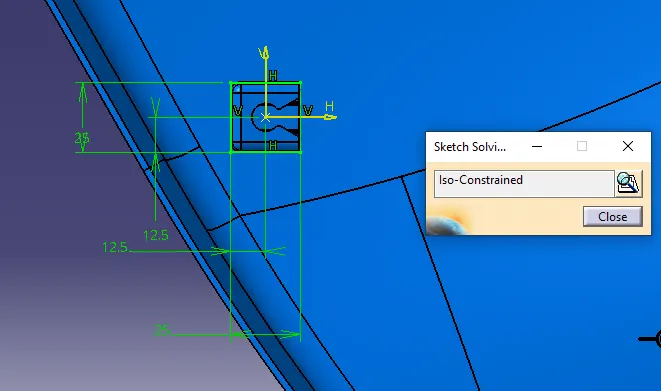
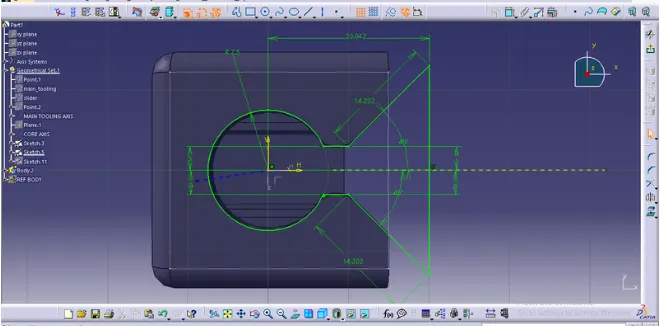
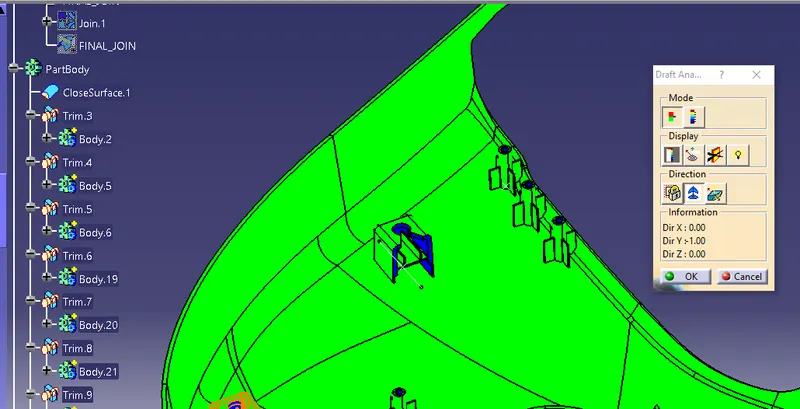
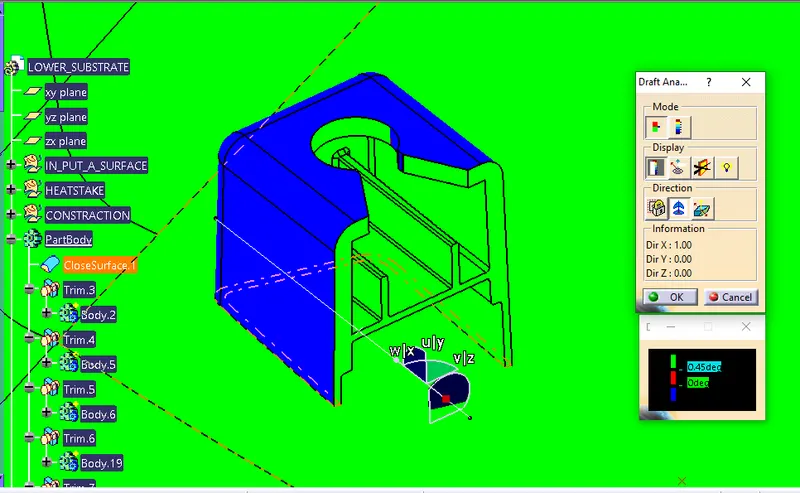
Create a straight line sketch using the surface as support.In the Surface workbench, Extrude the line in the direction of the Tooling axis.Trim the surfaces according to the required geometry.Go to the Part workbench and add Thickness to the extruded surface.
We now have a solid rib of definite volume and density.Give Draft of 0.5-1.5 degrees on all the vertical faces of the rib.This is done for easy ejection of the Core and to avoid any damage to the molded component.Select the faces to draft, neutral element, and pulling direction.
PUSH PIN :
Pushpin which helps us in Locating and Arresting components of an Assembly and it provides Alignment in Mating Parts and it also acts as a stopper or guide for various mechanisms.
DESIGN GUIDELINES FOR PUSH PIN
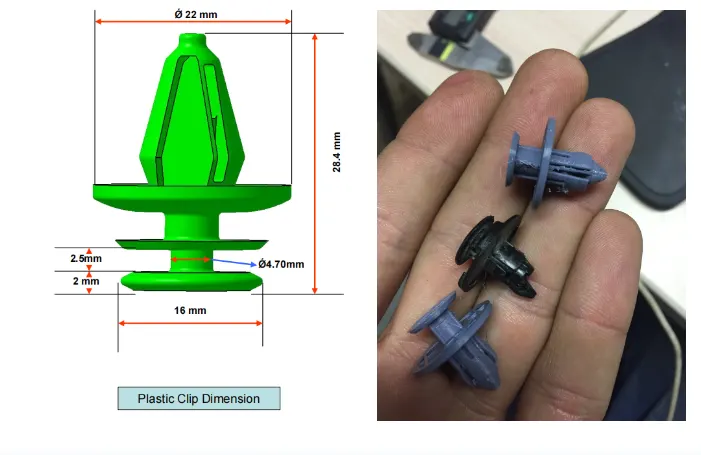
Draw the Boundary of the sketch to be revolved.Revolve the sketch about it's axis.There are some slots in the revolved geometry to facilitate as guideway for locating and arresting.Create a Rib sketch and then Pad it.Remove the Padded rib from the revolved geometry to get the desired shape of the pushclip.
or otherwise it is already provided on the given input
We provide rounded corners at edges to facilitate easy flow rate and avoid Flowlines.Min. Radius = 0.25 mm
- Heat stakes : In manufacturing products with thermoplastic components, it is often necessary to join a thermoplastic to a part of dissimilar material, whether it be metal, a dissimilar plastic, or other material. This technical information sheet provides design guidelines, configurations, and techniques for successful thermal (heat) staking.
GENERAL DESCRIPTION:
Thermal staking is an assembly method that uses the controlled melting and reforming of a
plastic stud or boss to capture or lock another plastic or metal component of an assembly in place.
The plastic stud protrudes through a hole in the component to be locked in place. The heated thermal tip contacts the top of the stud, which melts and fills the volume of the tip cavity to produce a head, locking the component in place.
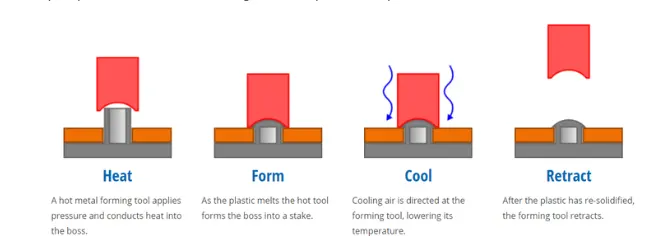
The progressive melting of plastic under continuous pressure forms the head.When staking, the right combination of heat and pressure for the application is critical.
ADVANTAGES:
- Simplification of machinery
- Reduced cost of machinery
- Multiple fastening points
- Allows higher density of welds compared to hot air cold form or ultrasonic welding
Design rules and construction procedure :
There are no standards for Dia,it depends on the manufacturer.The dimension is altered in such way that sink marks are avoided.There is no standard for thickness as well, but keep it lesser than the part thickness.Minimum 0.75mm at the Tip of the Rib.Molten material won't reach any further. give Height of Heatstake < Height of Locator Since Fixing occurs after Locating.
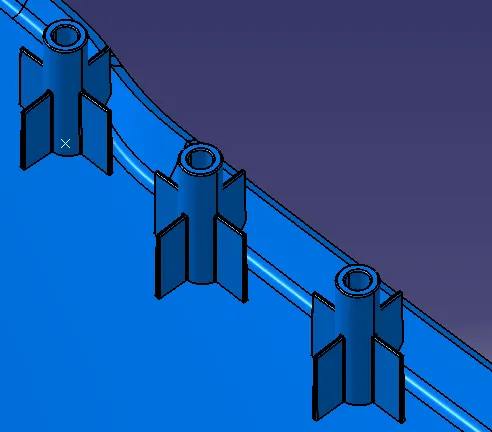
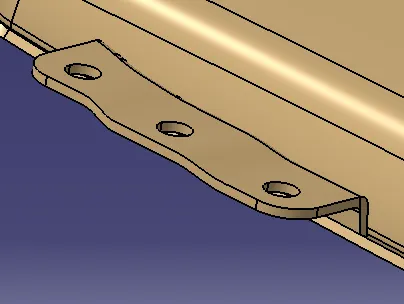
Flanges are created accoring to master section.
FINAL DRAFT ANALYSIS
Door Arm Rest
Map Pocket
Bottle holder
Lower Substrate
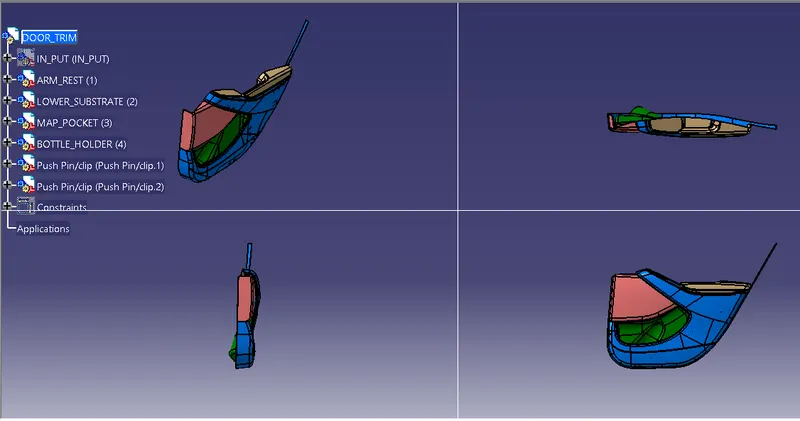
Final Model Images:
Conclusion :
- Class A, B and C surface was created as per the automotive standards using CATIA V5 Software.
- Draft Analysis was performed for the built model and it could be seen the the draft was under permissible limit for the manufacturing of the component.
- B side features were created for the component as per the design Rules.