Week 10 - Challenge 3 - Door Trim Lower with Engineering Features
AIM
- To Create the Door Trim Lower Plastic component through the given Class-A surface.
- To Create the Heat Stakes and the locators considering the design rules.
THEORY
Tooling Axis
Tooling Axis is the direction in which the mold or core and cavity opens and closes. While designing a component first thing is to define the tooling axis.
Procedure
- Check the connectivity of given Class A Surface i.e no gaps between the surfaces.
- Analyse the component along x,y,z direction and check which is the best possible tooling direction (Here Y)
- Create a point at flat surface by extracting it.
- Draw a line perpendicular to extracted flat surface through the point and that is the tooling axis.
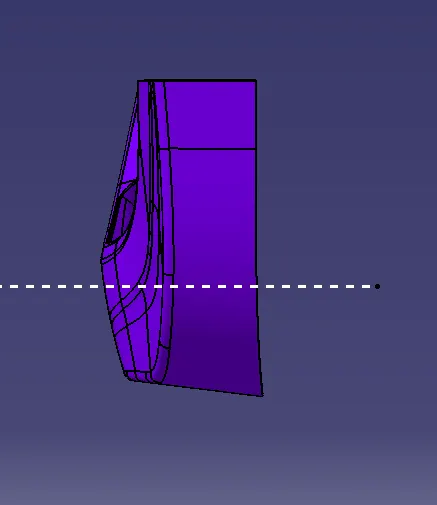
Tooling Axis By Bisecting Method
- Check the connectivity of given Class A Surface i.e no gaps between the surfaces.
- Analyse the component along x,y,z direction and check which is the best possible tooling direction (Here Y)
- Create a point at base surface by extracting it.
- Create an axis system with that point as origin.
- Create an intersection of class A in xy axis
- Create two lines with reference of faces which we think will create problems.
- Create a bisecting line with the lines drawn, which will gives us the tooling axis.
Draft Analysis
Draft analysis is used to analyze whether the part model created in CAD id manufacturable based on the draft condition applied.
Draft is required on all parts in the direction of mold movement in order to allow parts to release or eject from the mold properly. Most part or application require minimum `0.5^o - 1^o` as draft angle, however `3^o` is widely accepted as the norm.
Procedure
- First change the view to " Customize View Parameters" and select Material option.
- Select Feature Draft Analysis from the tool bar.
- Click on the direction, drag and drop the compass to the component such that it should coincide with the tooling axis.
- Lock the draft direction and click on the component.
- Green colour shows the positive draft, cyan as zero degree and red as negative draft
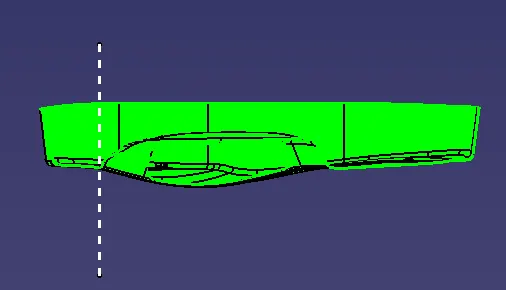
Heat Staking
In manufacturing products with thermoplastic components, it is often necessary to join a thermoplastic to apart of dissimilar material, whether it be a metal, dissimilar plastic or other material. This technical information sheet provides design guidelines, configurations and techniques for successful heat staking.
Thermal Staking or Heat staking is an assembly method that uses the controlled melting and reforming of plastic stud or boss to capture or lock another plastic or metal component of an assembly in place. The plastic stud protrudes through a hole in the component to be locked in place. The heated thermal tip contacts the top of stud, which melts and fills the volume of the tip cavity to produce a head, locking the component in place. The progressive melting of plastic under continuous pressure forms the head. When staking, the right combination of heat and pressure for the application is critical.
Heat staking also known as thermoplastic staking is the process of joining two dissimilar materials together. In heat staking we use local heating and cooling to raise the temperature of plastic components and allow plastic reforming to be carried out. This reforming can be used in a wide variety of applications.
Applications range from staking plastic boss’s for assembly of car door panels to joining PCB’s to plastic housings.
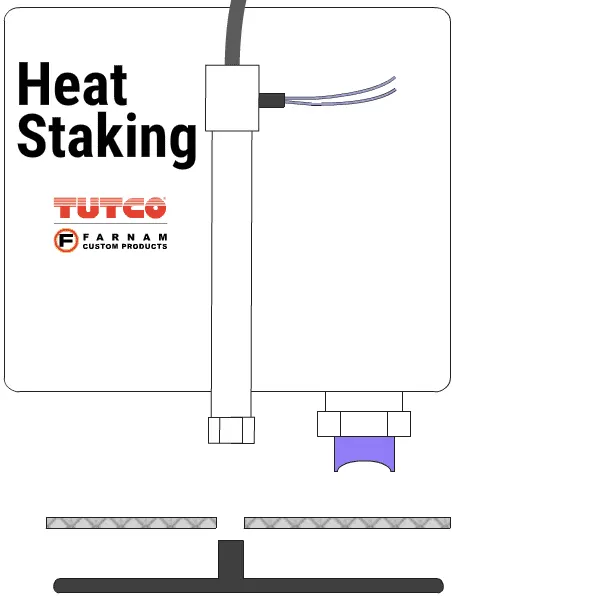
Advantages
- Simplification of machinery
- Reduced cost of machinery
- No vibration damage
- No particulates
- The ability to stake metalized coated applications
- The capability to stake in difficult to access or restricted areas.
- Multiple fastening points
- Allow higher density of welds compared to hot air cold form or ultrasonic welding.
Class A Surface: Class A surface is any of a set of freeform surfaces of high efficiency and quality. In other words, Class A surface is the aesthetic surface.
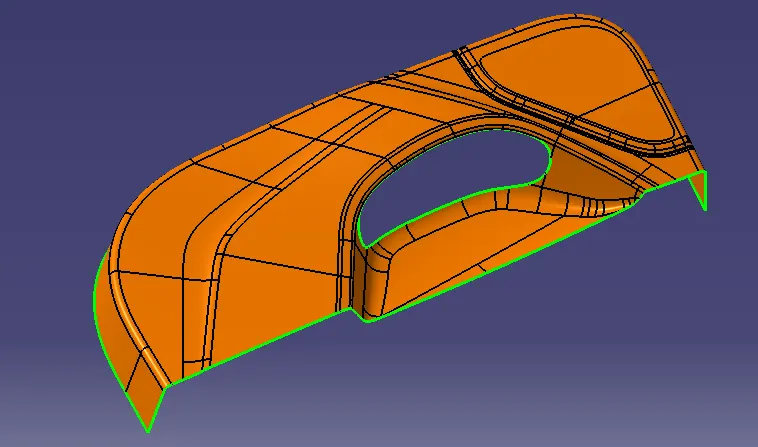
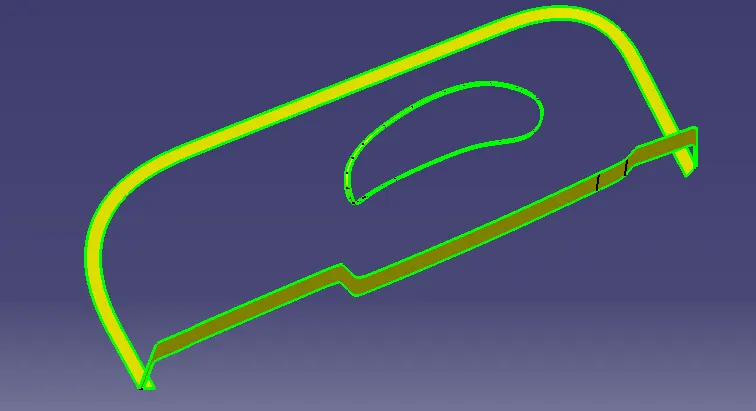
Class B Surface: Class B surface is the thickened suface or engineering surface where all ribs, screw bosses, dog houses etc will come.
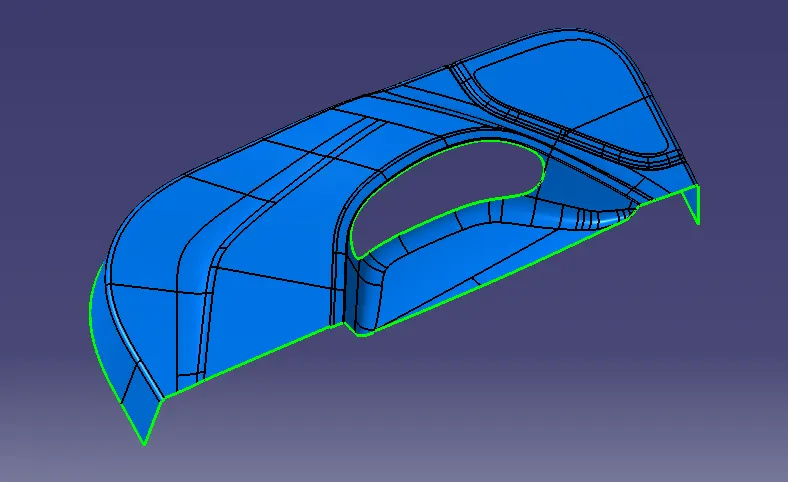
Class C Surface: It is the Surface which joins Class A and Class B surfaces.
SOFTWARE USED
Catia V5
DESIGN
Thickness T : 2.5mm
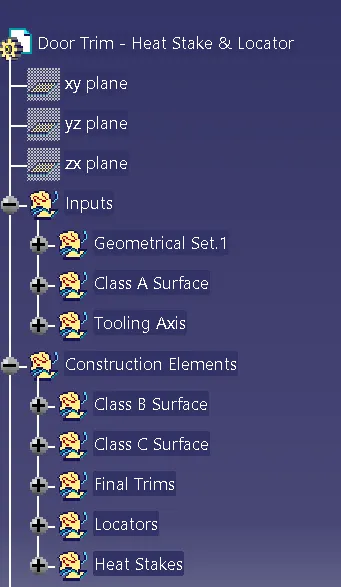
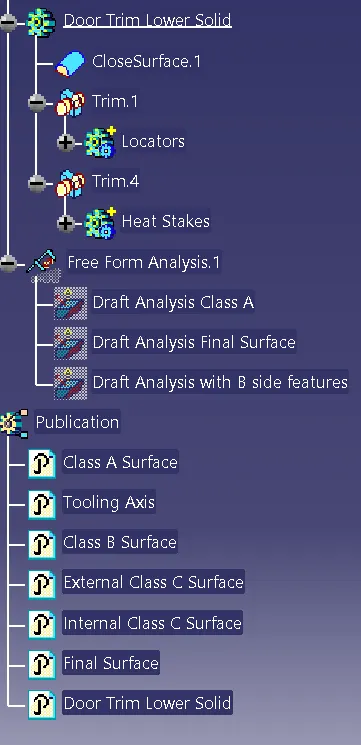
Tree Structure
Tooling Axis
Draft Analysis
Class A Surface
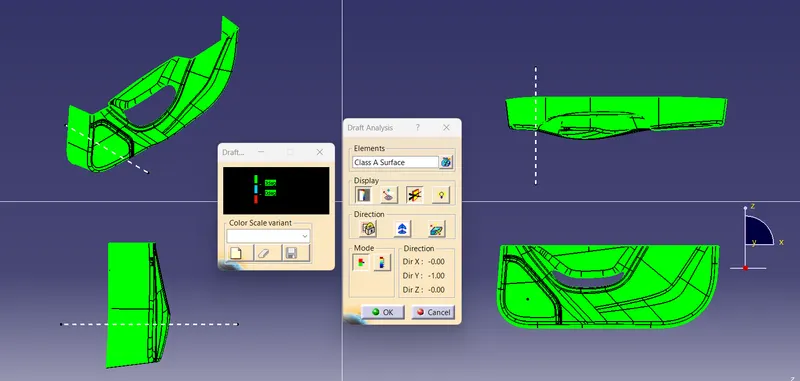
Final Closed Surface
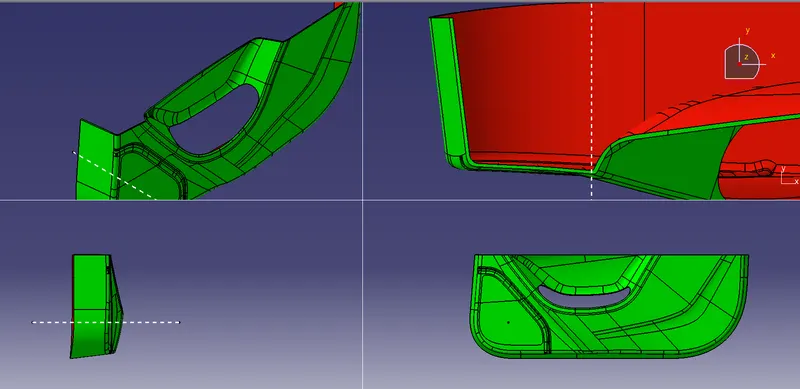
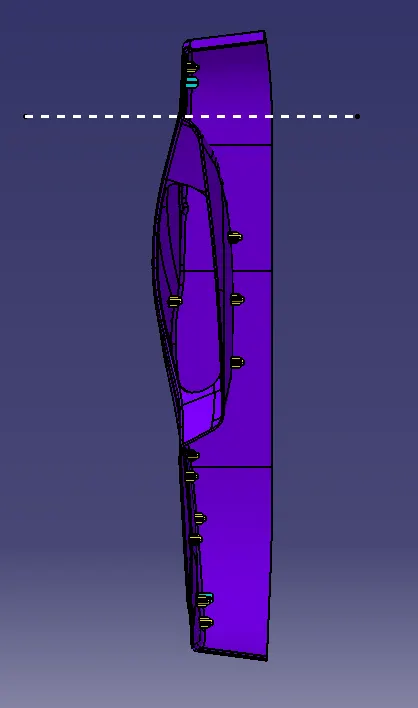
Final Component With B Side Features
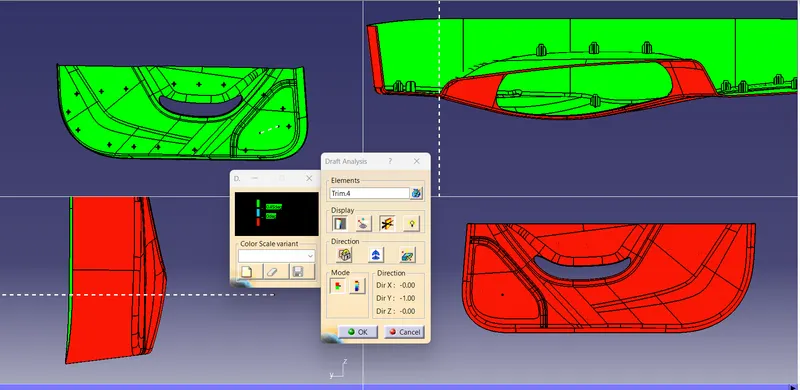
Class A Surface
Class B Surface
Class C Surface
Final Joined Surface
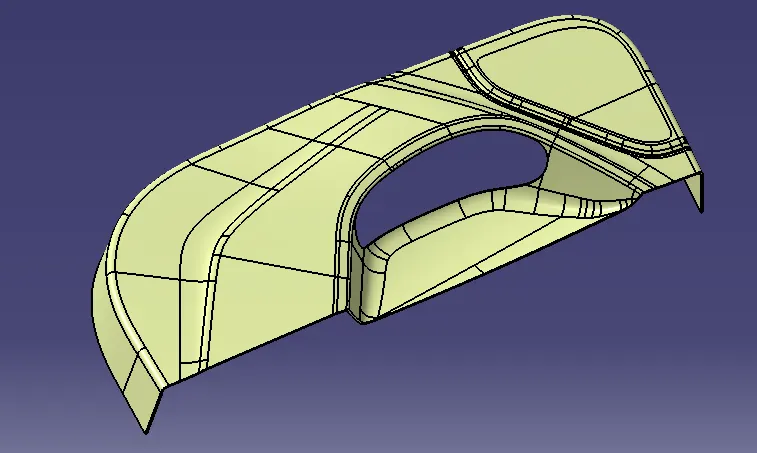
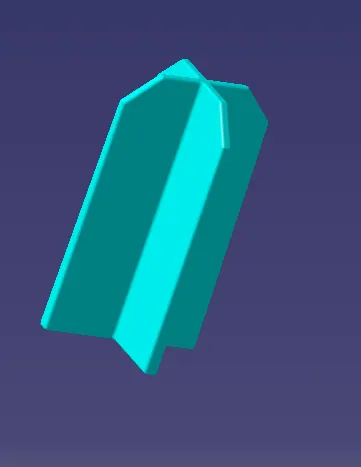
Locators
Sketch
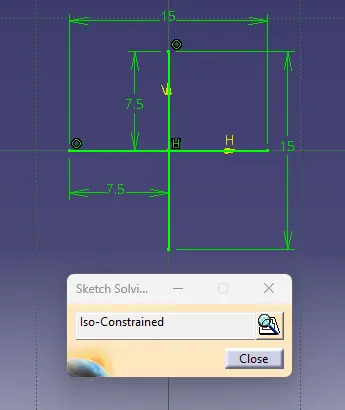
3D Model
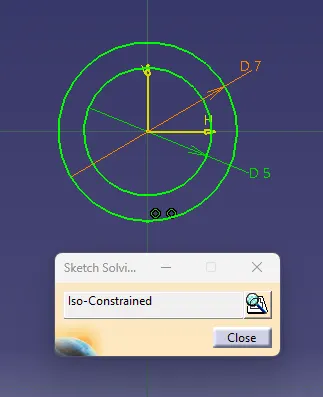
Heat Stakes
Sketch
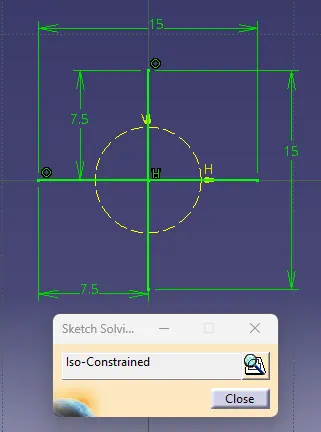
3D Model
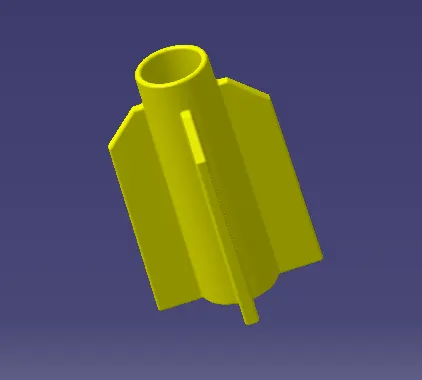
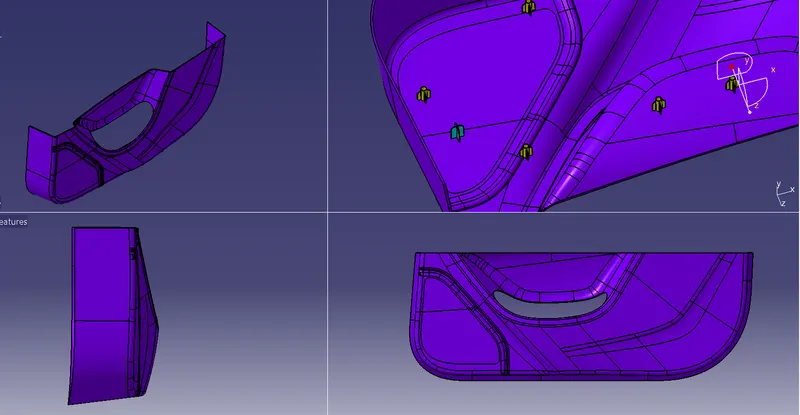
Final Component With Dog House In Various Orientations
Isometric View
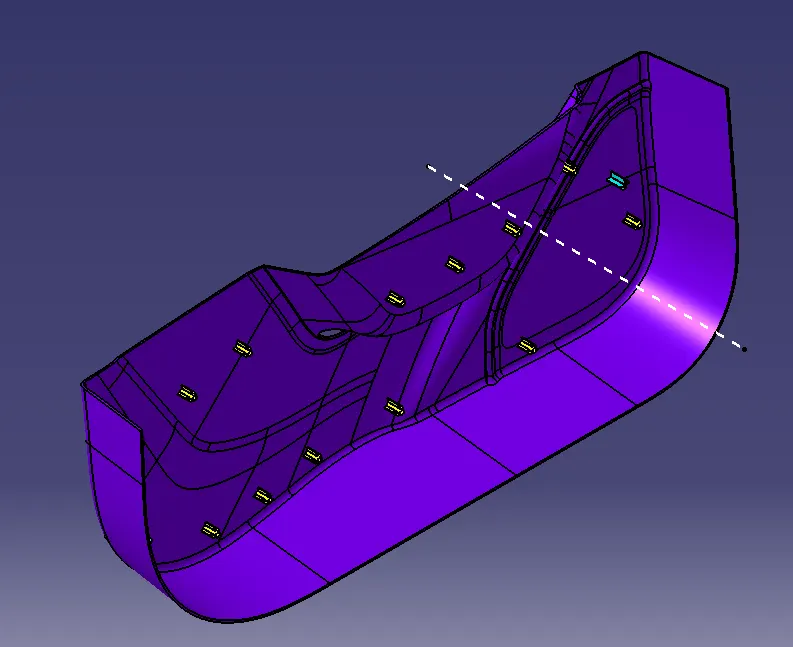
Front View
Left Side View
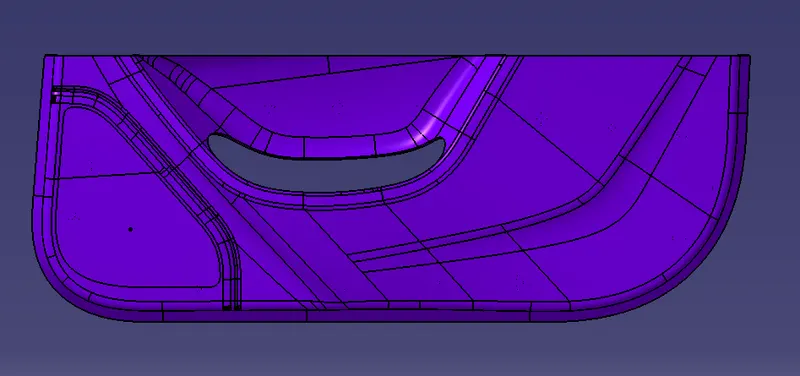
Right Side View
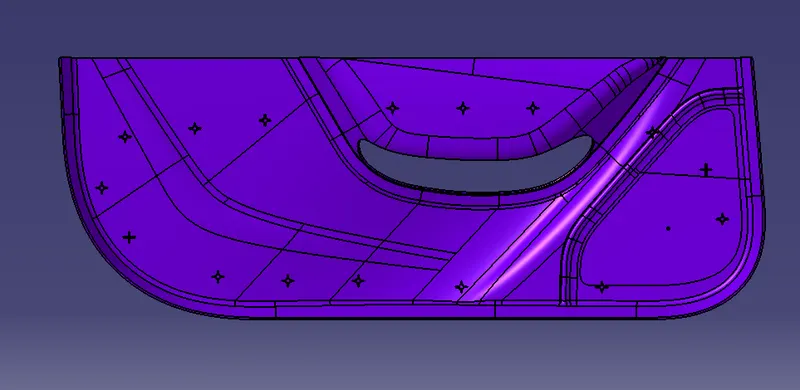
Top View
3D
CONCLUSION
Door Trim lower plastic component with Heat Stakes and the locators considering the design rules has been created in Catia.