Underbody Coating
UNDERBODY COATING:
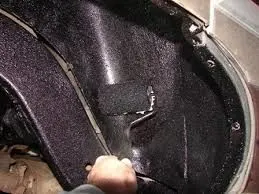
Underbody coating is a process to protect the car’s underbody from the corrosion. It also protects parts like internal body panels, frame rails and other inner cavities that are not physically accessible but are prone to corrosion.
PURPOSE:
- To protect against rust and corrosion
- Reduces NVH (Noise Vibrations Harshness) levels
- Prevent paint chipping
- Protects vital components
TYPES OF UNDERBODY COATING:
- Rubberized Undercoating
- Polyurethane Undercoating
- Wax or Paraffin-Based Undercoating
- Asphalt-Based Undercoating
(a) RUBBERIZED UNDERBODY COATING:
Rubberized undercoating’s do a great job of keeping existing rust all covered up and looking sharp, but it does absolutely nothing to slow down the spread of rust and corrosion sometimes the trapped air and moisture may even contribute to rust formation.
Uses: It is an easy-to-use black rubberized protective coating. It provides corrosion protection from water, salt and other chemicals. Its helps deaden sound and provides a barrier against rust on cars, trucks, trailers and other recreational vehicles.
(b)POLYURETHANE UNDERCOATING:
Polyurethane Undercoat may be top-coated with either acrylic or polyester urethane finishes and is especially formulated as an undercoat or sealer under AY&B Elite® Pro-Spray Linear Polyurethane and Elite® 321 Brushing Polyurethane finish coats.
(c)WAX OR PARAFFIN-BASED UNDERCOATING:
Wax or Paraffin-based undercoating’s have a wax inclusion that makes them stronger than water-based undercoating’s. Paraffin-based undercoating’s can be purchased through an automotive store in spray and paint-on formats. ... Paraffin-based undercoating needs to be replaced at least once a year at the vehicle owner's expense.
(d)ASPHALT-BASED UNDERCOATING:
Asphalt Based Undercoating does provide some benefits over Waxed Based Undercoating. They both stick well to most any surfaces and do a great job sealing out moisture, road chemicals and oxygen. But mainly, Asphalt undercoating has the benefit of being less expensive.
PROCESS OF UNDERBODY COATING:
PREHEAT TREATMENT:
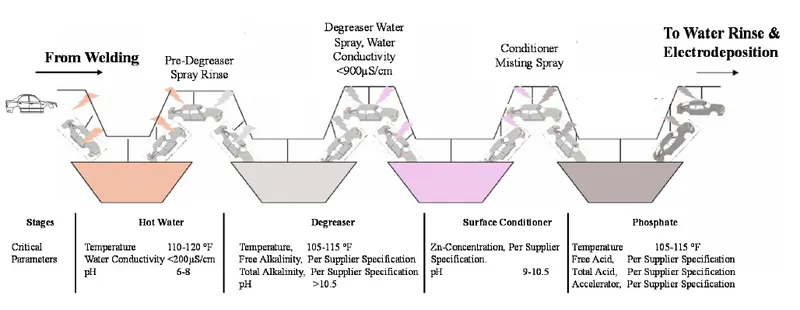
The first sequence in preparing the BIW for subsequent coating is pre-treatment Pre-heat treatment removes and clean excess metal and forms an appropriate surface structure enabling bonding of a corrosion protection layer. It consists of cleaning the body surface to remove remaining oils from the steaming process & welding residues through three primary liquid dip processes of degreasing, conditioning, & phosphating. Pre-treatment helps the primer to bond onto the metal. A phosphate treatment applies an inert layer of metal phosphate, providing resistance to corrosion spread. The degreasing solution is composed of alkaline salts and surfactants and can include caustic soda, sodium carbonate. The surfactants are types of detergents for emulsifying oils and lubricants on the BIW. In surface conditioner which creates nucleation sites for phosphate crystal growth. It increases the number of crystallization nuclei on the metal surface that enhance bonding mechanism for the subsequent phosphate sequence. Finally, the liquid dip phosphate ions, nitrate ions, zinc & hydrogen ions. The free acid etches the steel surface, causing hydrogen to be released while metal phosphate ions are precipitated onto the surface in a crystalline form
ELECTRODEPOSITION:
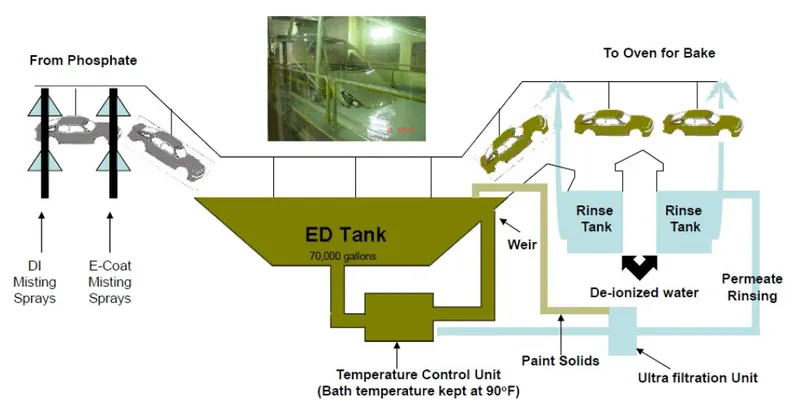
E-coating involves dipping automobile bodies into the coating solution & passing an electric current through the body & the liquid ED paint solution. Because of the charged nature of this coating process, the ED paint penetrates into places a spray would not reach. During operation, a mixture of resin, binder, & a paste containing the pigments is fed into the ED tank. The automobile body is lowered into the tank, and an electric current applied; the solution in the tank consists of 80-90% deionised water & 10-20% paint solids. The resin is the backbone of the final paint film & provides corrosion protection, durability, & toughness. Pigments are used to provide colour & gloss. After E-coat, the automobile body enters a bake oven, in which heating & keeping at a temperature of 160_C for 10 min causes film curing to promote maximum performance properties. The oven temperature & heating time primarily enhance chip resistance & film adhesion to the body; corrosion protected is affected less by these conditions. Because surface roughness influences the smoothness & brilliance of the topcoat, some sanding of the surface is usually performed to remove or eliminate defects before the body enters the next application step. A common challenge in the current E-coating process is that of water spots that contaminate coated surfaces. If water spots are present, they have removed by sanding. Hence, it is necessary to use well-deionized water & routinely monitor its conductivity. Alternately, operators also add surfactants or ultrafiltrates to the water
rinse zone to eliminate or manage water spots also add surfactants or ultrafiltrates to the water rinse zone to eliminate or manage water spots.
RUST-PROOF MATERIALS: SALER/PVC:
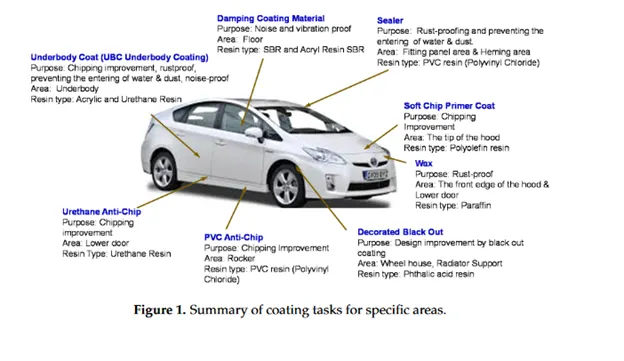
The third step is underbody coating & seam sealing using PVC. Fig.4 displays the lower door sections & rocker panel locations where PVC or urethanes are applied as an anti-chipping protection, & shows the cross section of this layer with respect to the other coatings on the body part During this third step, it is also typical to apply a soft tip primer coat that improves the chipping resistance . This layer is applied to the front edge of the hood, which is an area prone to chipping shock, using a high elastic resin that resides between the ED & primer coats. Also, during the third step, the radiator supports, wheel housing, & under rare areas of the body are coated with a relatively dull black pigment called a blackout coating.
PRIMER:
The fourth coating step is the primer. It can be water-borne, solvent-borne, or a powder. The primer fills & smooth minor imperfections & scratches that may be created during prior steps & by the intermediate sanding or grinding used to remove small imperfections. It also provides additional protection against corrosion & maximizes adhesion between it and the E-coat & basecoat; thereby, the Primer increases paint durability. Primer coating operations in an automobile assembly plant are usually implemented in three stages: Interior coating, Exterior coating, & then cutting in an oven. Manual spray painting is used for the interior coating of the doors, engine compartment, & luggage or trunk space. Some of the areas are not sprayed with basecoat. It is important that are primer colour matches the basecoat to be able to impart uniform coating appearances between interior & exterior coat.
TOPCOAT:
The final step in the body coating process is to apply the topcoat, which consists of two layers the basecoat & clearcoat.
Basecoat: It contains the primary colouring pigments. As part of the topcoat, the basecoat is third layer added to the car after the primer & before the clearcoat. It imparts the automobiles colour; roughly 40,000 base coat colour are known today , & approximately 1000 new colours are added to this list each year. Three different types of basecoats are used for automobiles, including solvent-borne medium solids (MS), solvent-borne high solids (HS), & water-borne.
Clearcoat: The final coating on an automobile surface is the clearcoat; it provides durability, environmental etch, & scratch resistance to the overall coating. It protects against damage such as fading that is caused by UV rays from the sun & imparts a gloss & depth that otherwise are not as vivid. The clearcoat also makes repairs & maintenance easier. Environmental etch is an appearance issue associated with the formation of
permanent water spots or non-removable marks from bird droppings, tree resin, or other chemicals after contact with an automobiles surface. The physical damage resulting from etch=ng is associated with a localized loss of material & deformation or pitting of the clearcoat surface.
NEED OF UNDERCOATING:
To maintain the thermal conductivity of the vehicle body.
To hide the body works which did during manufacturing, increasing the aesthetic look ad appearance of vehicle.
To improve vehicle acoustic performance, reducing road noise and structure-bome vibration noise, to provide a quieter ride for the both drivers and vehicle occupants.
Making a durable anti-stone and anti-chip coating to vulnerable parts of the vehicle. Helping to enhance corrosion performance of pre-applied coatings.
It has good resistance to abrasion and is over-paintable, making it a versatile option for many different areas on a vehicle.